EP2371721B1 - Behälter aus Kunststoff, insbesondere Flaschenkasten mit einem hohl ausgebildeten Handgriff sowie Verfahren zur Herstellung - Google Patents
Behälter aus Kunststoff, insbesondere Flaschenkasten mit einem hohl ausgebildeten Handgriff sowie Verfahren zur Herstellung Download PDFInfo
- Publication number
- EP2371721B1 EP2371721B1 EP11153200.8A EP11153200A EP2371721B1 EP 2371721 B1 EP2371721 B1 EP 2371721B1 EP 11153200 A EP11153200 A EP 11153200A EP 2371721 B1 EP2371721 B1 EP 2371721B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- handle
- wall
- profile support
- plastic
- gas injection
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 229920003023 plastic Polymers 0.000 title claims description 14
- 239000004033 plastic Substances 0.000 title claims description 14
- 238000004519 manufacturing process Methods 0.000 title description 6
- 238000002347 injection Methods 0.000 claims description 23
- 239000007924 injection Substances 0.000 claims description 23
- 238000001746 injection moulding Methods 0.000 claims description 6
- 238000000034 method Methods 0.000 claims description 5
- 238000000465 moulding Methods 0.000 claims description 5
- 238000004140 cleaning Methods 0.000 description 8
- 239000000155 melt Substances 0.000 description 4
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 4
- 230000015572 biosynthetic process Effects 0.000 description 3
- 238000010276 construction Methods 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 230000018109 developmental process Effects 0.000 description 1
- 239000007788 liquid Substances 0.000 description 1
- 230000000737 periodic effect Effects 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D1/00—Rigid or semi-rigid containers having bodies formed in one piece, e.g. by casting metallic material, by moulding plastics, by blowing vitreous material, by throwing ceramic material, by moulding pulped fibrous material or by deep-drawing operations performed on sheet material
- B65D1/22—Boxes or like containers with side walls of substantial depth for enclosing contents
- B65D1/24—Boxes or like containers with side walls of substantial depth for enclosing contents with moulded compartments or partitions
- B65D1/243—Crates for bottles or like containers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24012—Materials
- B65D2501/24019—Mainly plastics
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/2405—Construction
- B65D2501/24063—Construction of the walls
- B65D2501/2407—Apertured
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24197—Arrangements for locating the bottles
- B65D2501/24203—Construction of locating arrangements
- B65D2501/24261—Ribs on the side walls
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24363—Handles
- B65D2501/24369—Fixed, i.e. non swingable
- B65D2501/24401—Fixed, i.e. non swingable provided on a local area near to or at the upper edge or rim
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24363—Handles
- B65D2501/24509—Integral handles
- B65D2501/24522—Integral handles provided near to or at the uper edge or rim
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24363—Handles
- B65D2501/24509—Integral handles
- B65D2501/24535—Integral handles formed in the walls, e.g. roughnings, cavities or projections
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/2477—Parts reinforced
- B65D2501/24777—Side walls
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/24789—Means used for reinforcing
- B65D2501/24802—Hollow integral ribs
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/24828—Location of the reinforcing means
- B65D2501/24834—Inside the crate
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D2501/00—Containers having bodies formed in one piece
- B65D2501/24—Boxes or like containers with moulded compartments or partitions
- B65D2501/24006—Details relating to bottle crates
- B65D2501/24764—Reinforcements
- B65D2501/24828—Location of the reinforcing means
- B65D2501/24847—Oriented mainly vertically
Definitions
- the invention relates to a container made of plastic, in particular bottle crate according to the preamble of claim 1 and a method for producing such a container.
- Such plastic containers are usually formed by injection molding, for which purpose corresponding molds having a negative of the box to be formed having a mold cavity are used, into which hot plastic melt is injected.
- the cavity formation of a handle is often done by gas injection via a needle, the gas usually from the lower or inner edge of the handle, i. of the handle to be formed, is blown forth through channels in the tool.
- the needle is in the melt, and thus in the contour of the handle. In this case remains after production of the box, the Gaseinblasö réelle, which is felt when carrying the handle, which is disadvantageous.
- cleaning water can penetrate through the opening during the periodic cleaning process of such boxes, which in turn is disadvantageous, in particular also from a hygienic point of view. Because of this, such a gas injection opening is often closed in a final additional operation. However, additional operations slow down production and lead to higher prices.
- the object of the invention is to provide a corresponding container, in particular bottle crate, which is free from the described disadvantages of the prior art.
- the Gaseinblasö réelle is provided for the injection of gas for cavity formation of the handle in the handle laterally delimiting wall of the profile spar on the inside of the profile spar on the inner wall, wherein the Gaseinblasung takes place through the Gaseinblasö réelle in the handle laterally delimiting inner wall of the profile spar.
- the injection of the gas is no longer effected by means of a needle which dips into the melt, but preferably via an opening or mouth which is flush with the contour. In some cases, this mouth can be expediently slightly overhanging or reset. As a result, a closure of the opening is automatically given because nothing is in the contour. The opening closes automatically, but without additional work step.
- the handles are at least on one side preferably reinforced on both sides by hollow and from the upper edge of the box downwardly extending profile spars, which extend into the box interior from the inside of the side wall surface and are made by form of swords.
- the gas injection takes place from the side of the handle forth on the laterally adjoining wall surface on the handle, which has the advantage in hollow profile spars that the Gaseinblasö réelle is hidden to the outside, as it lies in the interior of the cavity of the profile spars.
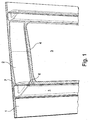
- FIG. 1 shows in partial view a side wall of a bottle crate, seen from the inside, which is formed in the usual manner of a box bottom and integrally formed circumferential four side walls and square or rectangular, but also has another floor plan.
- Such boxes have in at least one side wall or a plurality of side walls handles, which are usually formed by handles on the upper edge of the box.
- FIG. 1 shows a generally designated 1 side wall with a handle 2 above a display opening or handle opening 3 and an on both sides of the handle adjacent, in FIG. 1 only indicated hollow vertical spar 5, which extends from the bottom of the box substantially to the upper edge of the box. Such spars 5 are provided on both sides of the handle in the rule, as in particular from FIG. 2 evident.
- the profile struts 5 after FIG. 1 are formed in a conventional manner by forming blades, which extend into the injection molding cavity of the tool and are pulled out of the mold cavity after molding of the bottle crate, so that the hollow formation of a profile spar is formed.
- the gas injection takes place from the side of the handle or the handle ago in overlap with the handle and that according to FIG. 1 from the inside of the profile Holmes 5 ago, which has approximately triangular plan here.
- this opening is denoted by 6 by dashed lines.
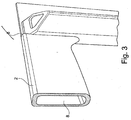
- This opening is introduced on the inner wall 7 of the profile struts 5 and approximately at the lower edge of the handle, but in overlap with the handle and leads directly in the direction of the handle, so that by appropriate gas injection in the handle 2, a cavity accordingly FIG. 3 is produced. There, the cavity is designated 8.
- the melt Since the cavity from the inside does not cool so quickly, and in this area, the melt is adjacent only outside of the tool and heat is dissipated, the melt remains liquid longer, and closes the injection hole independently.
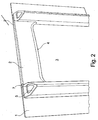
- FIG. 2 goes the hollow profile spar 5 in more detail. As FIG. 2 shows, these bars 5 are provided on both sides of the handle and close the edge of the handle or display opening 3, protrude inwardly beyond the side wall 1 and serve to stabilize the box in the region of the handle or display opening 3 and the handle second
Landscapes
- Engineering & Computer Science (AREA)
- Ceramic Engineering (AREA)
- Mechanical Engineering (AREA)
- Details Of Rigid Or Semi-Rigid Containers (AREA)
- Containers Having Bodies Formed In One Piece (AREA)
Description
- Die Erfindung betrifft einen Behälter aus Kunststoff, insbesondere Flaschenkasten gemäß dem Oberbegriff des Patentanspruches 1 sowie ein Verfahren zur Herstellung eines solchen Behälters.
- Derartige Kunststoffbehälter, insbesondere Flaschenkasten werden zumeist durch Spritzgießen gebildet, wozu entsprechende Formwerkzeuge mit einem das Negativ des zu formenden Kastens aufweisenden Formhohlraum verwendet werden, in welche heiße Kunststoffschmelze eingespritzt wird. Hierbei erfolgt die Hohlraumausbildung eines Handgriffs häufig durch Gaseinblasung über eine Nadel, wobei das Gas zumeist vom unteren oder inneren Rand des Handgriffes, d.h. des zu formenden Handgriffs, her über Kanäle im Werkzeug eingeblasen wird. Die Nadel steht dabei in der Schmelze, und somit in der Kontur des Handgriffs. Hierbei verbleibt aber nach Herstellung des Kastens die Gaseinblasöffnung, die bei Tragen des Handgriffs fühlbar ist, was nachteilhaft ist. Zudem kann über die Öffnung Reinigungswasser während des periodisch stattfindenden Reinigungsvorgangs derartiger Kasten eindringen, was wiederum nachteilhaft ist, insbesondere auch aus hygienischen Gesichtspunkten. Deswegen wird häufig eine solche Gaseinblasöffnung in einem abschließenden zusätzlichen Arbeitsvorgang verschlossen. Zusätzliche Arbeitsvorgänge verlangsamen aber die Herstellung und führen zu einer Verteuerung.
- Aus der
NL 8 903 105 WO 90/05 676 - Aufgabe der Erfindung ist es, einen entsprechenden Behälter, insbesondere Flaschenkasten zu schaffen, der frei von den beschriebenen Nachteilen des Standes der Technik ist.
- Diese Aufgabe wird erfindungsgemäß durch den Behältergemäß Anspruch 1 gelöst sowie durch das Verfahren gemäß Anspruch 2, wobei zweckmäßige Weiterbildungen sich aus dem Unteranspruch ergeben.
- Nach Maßgabe der Erfindung ist die Gaseinblasöffnung für die Gaseinblasung zur Hohlraumausbildung des Handgriffs in der den Handgriff seitlich begrenzenden Wand des Profilholms an der Innenseite des Profilholms an dessen Innenwand vorgesehen, wobei durch die Gaseinblasöffnung in der den Handgriff seitlich begrenzenden Innenwand des Profilholms die Gaseinblasung erfolgt. Das Einblasen des Gases erfolgt nicht mehr mittels einer Nadel die in die Schmelze eintaucht, sondern vorzugsweise über eine Öffnung oder Mündung welche bündig mit der Kontur abschließt. In einigen Fällen kann diese Mündung zweckmäßigerweise auch etwas überstehend oder zurückgesetzt sein. Dadurch ist ein Verschließen der Öffnung automatisch gegeben, da nichts mehr in die Kontur steht. Die Öffnung schließt selbsttätig, aber ohne zusätzlichen Arbeitsschritt. Hierbei sind zur Stabilität die Handgriffe Zumindest an einer Seite vorzugsweise beidseits durch hohle und vom oberen Kastenrand nach unten verlaufende Profilholme verstärkt, die sich in das Kasteninnere von der Innenseite der Seitenwandfläche her erstrecken und durch Formschwerter hergestellt sind. In diesen Fall erfolgt die Gaseinblasung von der Seite des Handgriffs her über die am Handgriff seitlich anschließende Wandfläche her, was bei Hohlprofilholmen den Vorteil hat, dass die Gaseinblasöffnung nach außen hin versteckt ist, da diese im Inneren des Hohlraums des Profilholme liegt.
- Nachfolgend wir ein bevorzugtes Ausführungsbeispiel der Erfindung anhand der Zeichnung beschrieben. Darin zeigen
- Fig. 1
- eine Teilansicht einer Seitenwand eines Flaschenkastens mit einem Handgriff, der beidseitig von vertikalen Hohlprofilholmen begrenzt ist, von denen beide Holme nur angedeutet sind,
- Fig. 2
- eine Ansicht entsprechend
Figur 1 , jedoch mit beidseitig dargestellten und mit der Seitenwand einstückig spritzgegossenen Holmen sowie - Fig. 3
- eine Teilansicht des Handgriffs von
Fig. 2 mit seitlichem Profilholm zur Darstellung der Hohlausbildung des Handgriffes. -
Figur 1 zeigt in Teilansicht eine Seitenwand eines Flaschenkastens, von innen her gesehen, der in der üblichen Weise aus einem Kastenboden und daran einstückig ausgebildeten umlaufenden vier Seitenwänden ausgebildet ist und quadratischen oder rechteckförmigen, aber auch anderen Grundriss aufweist. Derartige Kästen haben in mindestens einer Seitenwand oder mehreren Seitenwänden Griffe, die zumeist durch Handgriffe am oberen Kastenrand gebildet sind. -
Figur 1 zeigt eine allgemein mit 1 bezeichnete Seitenwand mit einem Handgriff 2 oberhalb einer Displayöffnung oder Handgrifföffnung 3 und einem beidseitg am Handgriff angrenzenden, inFigur 1 nur angedeuteten hohlen vertikalen Holm 5, der sich vom Kastenboden im Wesentlichen bis zum oberen Kastenrand erstreckt. Derartige Holme 5 sind beidseitig des Handgriffs in der Regel vorgesehen, wie insbesondere ausFigur 2 hervorgeht. - Die Profilholme 5 nach
Figur 1 sind in an sich bekannter Weise durch Formschwerter gebildet, die sich in den Spritzgusshohlraum des Werkzeugs erstrecken und nach Formung des Flaschenkastens aus dem Formhohlraum herausgezogen werden, so dass die hohle Ausbildung eines Profilholms entsteht. - Nach Maßgabe der Erfindung erfolgt die Gaseinblasung von der Seite des Handgriffs bzw. des Handgriffs her in Überdeckung mit dem Handgriff und zwar gemäß
Figur 1 von der Innenseite des Profilholmes 5 her, der hier etwa dreieckförmigen Grundriss aufweist. InFigur 1 ist diese Öffnung mit 6 bezeichnet und zwar durch strichlierte Linien. Diese Öffnung ist an der Innenwand 7 des Profilholme 5 eingebracht und etwa am unteren Rande des Handgriffs, aber in Überdeckung mit dem Handgriff und führt unmittelbar in Richtung des Handgriffes, so dass durch entsprechende Gaseinblasung im Handgriff 2 ein Hohlraum entsprechendFigur 3 erzeugt wird. Dort ist der Hohlraum mit 8 bezeichnet. - Da der Hohlraum von innen nicht so schnell abkühlt, und in diesem Bereich die Schmelze nur außen am Werkzeug angrenzt und Wärme abgeführt wird, bleibt die Schmelze länger flüssig, und verschließt das Einblasloch selbstständig.
- Dies hat zur Folge, dass sich nach Gaseinblasung die Öffnung 6 von selbst verschließt infolge des noch weichen Kunststoffs, so dass in einem späteren Reinigungsvorgang Reinigungswasser nicht eindringen kann. Zudem ist selbst für den Fall, dass die Öffnung nicht bzw. nicht vollständig verschlossen wird, diese nach außen hin versteckt und wird in der Regel während des Reinigens des Flaschenkastens nicht durch Reinigungswasser gefüllt.
- Aus
Figur 2 geht der hohle Profilholm 5 genauer hervor. WieFigur 2 zeigt, sind diese Holme 5 beidseitig des Handgriffs vorgesehen und schließen randseitig die Handgriffoder Displayöffnung 3 ab, ragen nach innen über die Seitenwand 1 vor und dienen zur Stabilisierung des Kastens im Bereich der Handgriff oder Displayöffnung 3 und des Handgriffs 2. - Die.Herstellung derartiger Kästen erfolgt durch Spritzgießen aus Kunststoff in einen Formhohlraum, in den entsprechende Formschwerter hineintauchen, um die Holme auszubilden. Zumeist vom Boden her, oftmals aber auch von verschiedenen Stellen her, erfolgt das Einspritzen von Kunststoff und zwar Kunststoffschmelze zur Herstellung des Flaschenkastens.
- Infolge des im Bereich der Gaseinblasöffnung noch heißen Kunststoffs erfolgt nach Gaseinspritzung und Formung des Griffhohlraums ein selbsttätiges Verschließen der Gaseinblasöffnung, die im Übrigen ohnedies innerhalb des Handgriffs versteckt ist. Selbst für den Fall, dass die Gaseinblasöffnung also nicht geschlossen wird, würde ein Zutritt von Reinigungswasser während des Reinigungsvorgangs in den Handgriff verringert werden. Eine verbleibende Gaseinblasöffnung wäre damit entsprechend versteckt und würde im Übrigen beim Tragen des Handgriffs auch nicht gefühl werden können.
Claims (3)
- Behälter aus Kunststoff, insbesondere Flaschenkasten, mit einem Boden und mit vorzugsweise vier umlaufend angeordneten Seitenwänden, wobei in mindestens einer Seitenwand (1) ein Griff ausgebildet ist, der durch einen quer zu den durch benachbarte Seitenwände gebildete vom Boden zum oberen Behälterrand verlaufenden Ecken gerichteten Handgriff (2) gebildet ist, der zumindest an einer Seite, vorzugsweise beidseitig, durch einen hohlen über ein Formschwert während des Spritzgießens gebildeten Profilholm (5) begrenzt ist, dadurch gekennzeichnet, dass der Profilholm (5) jeweils eine den Handgriff (2) seitlich begrenzende Wand bildet bzw. beinhaltet, wobei
in der den Handgriff seitlich begrenzenden Wand des Profilholms an einer Innenwand (7) des Profilholms (5) und in Überdeckung mit dem Handgriff (2) eine Gaseinblasöffnung (6) für eine Gaseinblasung zur Hohlraumausbildung des Handgriffs vorhanden ist, die unmittelbar in Richtung des Handgriffs führt, wobei durch die Gaseinblasöffnung (6) in der den Handgriff (2) seitlich begrenzenden Innenwand (7) des Profilholms (5) von einer Innenseite des Profilsholms (5) her Gas in den Handgriff (2) eingeblasen ist, wodurch im Handgriff ein Hohlraum ausgebildet ist. - Verfahren zu Herstellung eines Behälters aus Kunststoff, inbesondere Flaschenkastens, nach Anspruch 1,
dadurch gekennzeichnet, dass
die Gaseinblasung zur Bildung des Griffhohlraums an der den Handgriff (2) seitlich begrenzenden Innenwand (7) des Profilholms von der Innenseite des Profilholms her erfolgt, und sich die seitlich am Handgriff (2) in der begrenzenden Wand befindliche Gaseinblasöffnung (6), vorzugsweise durch die in diesem Bereich noch heiße Kunststoffschmelze selbsttätig, nach der Gaseinblasung und Bildung des Formhohlraums des Handgriffes (2) schließt, wobei die Gaseinblasung vom seitlichen Rand des Handgriffs (2) her in seitlicher Überdeckung des durch Spritzgießen des mit dem Behälter geformten Handgriffes (2)erfolgt, wobei die den Handgriff (2) begrenzenden seitlichen Profilholme (5) durch Formschwerter gebildet sind. - Verfahren zu Herstellung eines Behälters aus Kunststoff nach Anspruch 2,
dadurch gekennzeichnet, dass die Formschwerter in den Formhohlraum für das Spritzgießen des Kunststoffs vorstehen.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE201010013704 DE102010013704A1 (de) | 2010-04-01 | 2010-04-01 | Behälter aus Kunststoff, insbesondere Flaschenkasten mit einem hohl ausgebildeten Handgriff sowie Verfahren zur Herstellung |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2371721A1 EP2371721A1 (de) | 2011-10-05 |
| EP2371721B1 true EP2371721B1 (de) | 2016-04-13 |
Family
ID=44083484
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP11153200.8A Not-in-force EP2371721B1 (de) | 2010-04-01 | 2011-02-03 | Behälter aus Kunststoff, insbesondere Flaschenkasten mit einem hohl ausgebildeten Handgriff sowie Verfahren zur Herstellung |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP2371721B1 (de) |
| DE (1) | DE102010013704A1 (de) |
| PL (1) | PL2371721T3 (de) |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE8915831U1 (de) * | 1988-11-08 | 1991-09-26 | Schoeller International Engineering KG Sparrenberg, Unterengstringen | Flaschenkasten aus Kunststoff |
| NL8902264A (nl) * | 1989-09-11 | 1991-04-02 | Wavin Bv | Flessenkrat. |
| NL8903105A (nl) * | 1989-12-19 | 1991-07-16 | Wavin Bv | Kunststofkrat met holle kolommen voorzien van een gasinjektieopening, alsmede werkwijze en inrichting voor het vervaardigen van een dergelijke kunststofkrat. |
| DE10016973A1 (de) * | 2000-04-06 | 2001-10-11 | Oberland Engineering Gmbh | Verfahren zum Herstellen eines Handgriffs, danach hergestellte Handgriffe und Flaschenkasten mit einem Handgriff |
-
2010
- 2010-04-01 DE DE201010013704 patent/DE102010013704A1/de not_active Ceased
-
2011
- 2011-02-03 EP EP11153200.8A patent/EP2371721B1/de not_active Not-in-force
- 2011-02-03 PL PL11153200.8T patent/PL2371721T3/pl unknown
Also Published As
| Publication number | Publication date |
|---|---|
| DE102010013704A1 (de) | 2011-10-06 |
| EP2371721A1 (de) | 2011-10-05 |
| PL2371721T3 (pl) | 2016-10-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102012003219B4 (de) | Kunststoffbehältnis | |
| EP0490165B1 (de) | Transportbehälter, insbesondere Flaschenkasten aus Kunststoff | |
| DE20313077U1 (de) | Transportkasten aus Kunststoff | |
| EP2783999B1 (de) | Teilbarer Behälter, insbesondere Flaschenkasten | |
| EP0396728B2 (de) | Flaschenkasten aus kunststoff | |
| DE60305838T2 (de) | Spritzgiessverfahren zum Herstellen eines Kunststoffbehälters oder Kunststoffverschlusses mit unten umgebördeltem Öffnungsrand | |
| EP4255818A1 (de) | Kunststoffbehälter mit verstärkten eckpartien | |
| DE10239319B4 (de) | Zweikomponenten Kunstoffbehälter | |
| DE3900894A1 (de) | Verfahren zur herstellung von flaschenkaesten mit waagrechten griffholmen sowie entsprechende flaschenkaesten | |
| EP2371721A1 (de) | Behälter aus Kunststoff, insbesondere Flaschenkasten mit einem hohl ausgebildeten Handgriff sowie Verfahren zur Herstellung | |
| DE60301134T2 (de) | Behälter, daraus hergestellte verpackung und formwerkzeug und verfahren zur herstellung des behälters | |
| EP2383190B1 (de) | Transportbehälter zur Aufnahme von insbesondere Lebensmitteln | |
| EP3218278B1 (de) | Behälter mit lüftungskanal | |
| DE19525000C1 (de) | Spritzgießwerkzeug zur Herstellung eines aus Kunststoff bestehenden Kastens | |
| EP2633968B1 (de) | Verfahren zum Herstellen eines Kunststoffbehälters und Kunststoffbehälter | |
| EP0484763B1 (de) | Verfahren und Vorrichtung zur Herstellung von Transportkästen, insbesondere Flaschenkästen | |
| DE102015102307A1 (de) | Kasten aus Kunststoff, insbesondere Flaschenkasten | |
| DE102016118495A1 (de) | Kunststoffbehältnis und Boden für ein Kunststoffbehältnis | |
| DE202007003595U1 (de) | Verschlusselement für einen Kunststoffdeckel | |
| DE20013467U1 (de) | Formwerkzeug für Spritzgießbauteile | |
| WO2025108845A1 (de) | Behälter, behälteranordnung sowie verfahren zum herstellen eines behälters | |
| EP4159401A1 (de) | Verfahren zum herstellen eines vor-formlings und vor-formling | |
| DE3839087A1 (de) | Flaschenkasten aus kunststoff sowie verfahren zur herstellung desselben | |
| DE102006048569A1 (de) | Transportkasten aus Kunststoff, insbesondere für den Transport von Flaschen, und ein Verfahren zu seiner Herstellung | |
| DE1479200A1 (de) | Verfahren und Vorrichtung zum Herstellen von Flaschen aus warmformbarem Kunststoff und zum Abtrennen abgequetschten Materials |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20110722 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| 17Q | First examination report despatched |
Effective date: 20130624 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SCHOELLER ALLIBERT GMBH |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20150917 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 789835 Country of ref document: AT Kind code of ref document: T Effective date: 20160415 Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502011009399 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: FP |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160713 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160816 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160714 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502011009399 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| 26N | No opposition filed |
Effective date: 20170116 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20170203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170228 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170228 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20171031 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170203 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20190219 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CZ Payment date: 20190129 Year of fee payment: 9 Ref country code: PL Payment date: 20190124 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20190215 Year of fee payment: 9 Ref country code: BE Payment date: 20190219 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20110203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160413 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160813 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20200429 Year of fee payment: 10 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20200301 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 789835 Country of ref document: AT Kind code of ref document: T Effective date: 20200203 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20200229 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200203 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200301 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200229 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502011009399 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210901 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200203 |