EP1010624A2 - Method of cleaning a gumming device - Google Patents
Method of cleaning a gumming device Download PDFInfo
- Publication number
- EP1010624A2 EP1010624A2 EP99124651A EP99124651A EP1010624A2 EP 1010624 A2 EP1010624 A2 EP 1010624A2 EP 99124651 A EP99124651 A EP 99124651A EP 99124651 A EP99124651 A EP 99124651A EP 1010624 A2 EP1010624 A2 EP 1010624A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- tank
- gumming
- conduit
- substance
- adhesive substance
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C9/00—Details of labelling machines or apparatus
- B65C9/20—Gluing the labels or articles
- B65C9/22—Gluing the labels or articles by wetting, e.g. by applying liquid glue or a liquid to a dry glue coating
- B65C9/2247—Gluing the labels or articles by wetting, e.g. by applying liquid glue or a liquid to a dry glue coating using liquid rollers or bands
Definitions
- the present invention relates to a method of cleaning a gumming device.
- the present invention relates to a method of cleaning a gumming device for gumming sheets of packing material on product packing machines, to which the following description refers purely by way of example.
- the packing material is gummed using gumming devices fitted to the machines themselves and each normally comprising at least one gumming roller partially immersed in an adhesive substance inside a tank, and which, during the gumming operation, is brought into contact with the strip material for gumming; and a supply circuit for feeding the adhesive substance from a storage vessel to the tank.
- gumming devices fitted to the machines themselves and each normally comprising at least one gumming roller partially immersed in an adhesive substance inside a tank, and which, during the gumming operation, is brought into contact with the strip material for gumming; and a supply circuit for feeding the adhesive substance from a storage vessel to the tank.
- the gumming roller of gumming devices of the above type must be cleaned to remove the dried adhesive substance off the surface of the roller.
- cleaning involves dismantling the entire gumming device off the packing machine, and transferring the device to the maintenance area.
- dismantling the gumming device may also result in damage to the device itself.
- a method of cleaning a gumming device during a pause in the operating cycle of the gumming device comprising a gumming roller partially immersed in an adhesive substance inside a tank; and the method being characterized by comprising the steps of emptying said tank of said adhesive substance during said pause; at least partially filling the tank with a liquid solvent substance; and washing said gumming roller with the solvent substance.
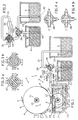
- Number 1 in Figure 1 indicates a unit for cleaning a gumming device 2 for applying an adhesive substance 3 to sheets 4 of packing material, which are fed successively, each with a respective surface 5 facing downwards, along a path 6 defined by the periphery 7 of a conveying roller 8 of a packing machine 9.
- Roller 8 is fitted to a powered shaft 10 to rotate about a respective axis 11 crosswise to the traveling direction 12 of sheets 4 along path 6.
- Gumming device 2 comprises a container 13, substantially in the form of a cup-shaped right parallelepipedon, which in turn comprises a front wall 14 and a rear wall 15, both vertical and parallel to each other, two end walls 16 (only one shown in Figure 1) parallel to each other and perpendicular to walls 14 and 15, and a bottom tank 17 containing adhesive substance 3.
- Container 13 houses a gumming roller 18, which rotates, clockwise in Figure 1, about an axis 19 parallel to axis 11 of roller 8, and is located on the opposite side of path 6 to roller 8.
- Gumming roller 18 is defined externally by a substantially cylindrical gumming surface 20, a top portion 21 of which is tangent, at a gumming station 22, to path 6 of sheets 4 and projects from an opening 23 formed through a cover 24 fitted to the top ends of walls 14, 15 and 16 to close container 13; and a bottom portion 25 of gumming roller 18 is immersed inside tank 17.
- Container 13 also houses a scraper 26, which comprises an end 27 connected to wall 14, and an end, opposite end 27, defined by a U-shaped blade 28 having an edge 29 substantially contacting a generating line of surface 20 of gumming roller 18.
- gumming device 2 comprises a circuit 30 for supplying adhesive substance 3, and which in turn comprises a tubular conduit 31 and a supply pump 35 connected to conduit 31.
- One end 32 of conduit 31 is immersed in adhesive substance 3 inside a storage tank 33 for adhesive substance 3, and another end 34 of conduit 31 communicates with tank 17.
- pump 35 is a known reversible supply pump, i.e. can be operated to draw and feed adhesive substance 3 from tank 33 to tank 17 along conduit 31 in the direction of arrow F1 in Figure 1, or to draw and feed adhesive substance 3 from tank 17 to tank 33 along conduit 31 in the direction of arrow F2, opposite the direction of arrow F1, in Figure 1.
- circuit 30 comprises a supply pump 36, and a known direction valve 37 connected to conduit 31 downstream from pump 36 with reference to the direction indicated by arrow F1 in Figure 1.
- Valve 37 has four inlet/outlet holes A,B,C,D, which are selectively positioned to communicate in pairs A-B and C-D or D-B and C-A to define respective pairs of connections AB-CD, DB-CA to conduit 31 corresponding to two different operating positions of valve 37 shown in Figures 3a and 3b respectively.
- valve 37 When valve 37 is in the Figure 3a operating position, adhesive substance 3 flows along conduit 31 in the direction indicated by arrow F1 in Figure 1, i.e. pump 36 draws and feeds adhesive substance 3 from tank 33 to tank 17; and, when valve 37 is in the Figure 3b operating position, adhesive substance 3 flows along conduit 31 in the direction indicated by arrow F2, opposite to F1, in which pump 36 draws and feeds adhesive substance 3 from tank 17 to tank 33.
- Unit 1 comprises a further known direction valve 38 connected to conduit 31 between end 32 and pump 35 in the Figure 1 embodiment, or between end 32 and the inlet/outlet A of valve 37 in the Figure 2 embodiment.
- Valve 38 has three inlet/outlet holes A',B',C', hole A' of which is connected to a tubular conduit 39 having an end 40 immersed in a tank 41 of a liquid solvent substance 42.
- holes A',B',C' of valve 38 are selectively positioned to communicate in pairs B'-C' or A'-C' to define a connection B'-C' to conduit 31 or a connection A'-C' to conduit 39, corresponding to two different operating positions of valve 38 shown in Figures 4a and 4b respectively.
- Unit 1 also comprises a known automatic control device 43 connected to pump 35 and valve 38 in the Figure 1 embodiment, or to valves 37, 38 and pump 36 in the alternative Figure 2 embodiment, and which provides for controlling operation of pump 35 and valve 38, or operation of valves 37, 38 and pump 36, according to a given sequence.
- a known automatic control device 43 connected to pump 35 and valve 38 in the Figure 1 embodiment, or to valves 37, 38 and pump 36 in the alternative Figure 2 embodiment, and which provides for controlling operation of pump 35 and valve 38, or operation of valves 37, 38 and pump 36, according to a given sequence.
- device 43 preferably controlled by a timing device not shown, activates the emptying of tank 17 by operating pump 35, or setting valve 37 to the Figure 3b operating position, to transfer adhesive substance 3 into tank 33.
- device 43 sets valve 38 to the Figure 4b position, and either activates pump 35 in the reverse suction position, or sets valve 37 to the Figure 3a position and activates pump 36, so that solvent substance 42 flows along conduit 31 from tank 41 to tank 17, which is gradually filled so that gumming roller 18 is partially immersed in solvent substance 42.
- gumming roller 18 is put through a wash cycle by rotating gumming roller 18 about axis 19.
- device 43, valve 38 and conduit 39 of unit 1 are dispensed with, and the above operations are controlled by a maintenance worker who activates the emptying of tank 17 and, once adhesive substance 3 is transferred from tank 17 to tank 33, manually substitutes tank 41 of liquid solvent substance 42 for tank 33, immerses end 32 of conduit 31 in solvent substance 42, and either activates pump 35, or valve 37 followed by pump 36, so that solvent substance 42 flows from tank 41 to tank 17.
- a maintenance worker who activates the emptying of tank 17 and, once adhesive substance 3 is transferred from tank 17 to tank 33, manually substitutes tank 41 of liquid solvent substance 42 for tank 33, immerses end 32 of conduit 31 in solvent substance 42, and either activates pump 35, or valve 37 followed by pump 36, so that solvent substance 42 flows from tank 41 to tank 17.
- gumming roller 18 is cleaned, tank 41 is removed and tank 33 replaced in the operating position.
- gumming roller 18 is thus cleaned thoroughly and quickly without dismantling device 2 from packing machine 9.
- unit 1 as described above also provides for rapid cleaning of gumming roller 18 even in the event of short stoppages of machine 9, to prevent portions of adhesive substance 3 forming on surface 20 of gumming roller 18.
Landscapes
- Cleaning In General (AREA)
- Detergent Compositions (AREA)
- Coating Apparatus (AREA)
Abstract
Description
Claims (6)
- A method of cleaning a gumming device during a pause in the operating cycle of the gumming device; the gumming device (2) comprising a gumming roller (18) partially immersed in an adhesive substance (3) inside a tank (17); and the method being characterized by comprising the steps of emptying said tank (17) of said adhesive substance (3) during said pause; at least partially filling the tank (17) with a liquid solvent substance (42); and washing said gumming roller (18) with the solvent substance (42).
- A method as claimed in Claim 1, characterized in that said gumming device (2) has a feed circuit (30) for feeding said adhesive substance (3) to said tank (17) from a storage tank (33) containing the adhesive substance (3).
- A method as claimed in Claim 2, characterized in that said emptying step comprises the step of transferring the adhesive substance (3) in said tank (17) to said storage tank (33).
- A method as claimed in Claim 3, characterized in that said filling step comprises the steps of connecting a storage tank (41) containing said solvent substance (42) to said circuit (30); and transferring the solvent substance (42) from said storage tank (41) to said tank (17).
- A method as claimed in any one of Claims 2 to 4, characterized in that said feed circuit (30) comprises a first tubular supply conduit (31) communicating with said storage tank (33) of adhesive substance (3) and with said tank (17); a reversible supply pump (35) connected to said first tubular conduit (31); a direction valve (38) connected to said first tubular supply conduit (31) and having three inlet/outlet holes (A',B',C') selectively positioned to communicate in pairs (B'C'; A',C'); and a second tubular conduit (39) connected to one (A') of said inlet/outlet holes (B'C'; A'C') of said valve (38) and having one end (40) inside said storage tank (41) of said solvent substance (42); said transfer step being performed along said first tubular conduit (31) by means of said reversible pump (35) and via said direction valve (38).
- A method as claimed in any one of claims 2 to 4, characterized in that said feed circuit (30) comprises a first tubular supply conduit (31) communicating with said storage tank (33) of adhesive substance (3) and with said tank (17); a supply pump (36) connected to said first tubular conduit (31); a first direction valve (38) connected to said first tubular supply conduit (31) and having three inlet/outlet holes (A',B',C') selectively positioned to communicate in pairs (B'C'; A',C'); a second tubular conduit (39) connected to one (A') of said inlet/outlet holes (B'C'; A'C') of said first valve (38) and having one end (40) inside said storage tank (41) of said solvent substance (42); and a second direction valve (37) connected to said first conduit (31) and having four inlet/outlet holes (A,B,C,D) selectively positioned to communicate in pairs (AB,CD; DB,CA); said transfer step being performed along said first tubular conduit (31) by means of said pump (36) and via said direction valves (37, 38).
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT1998BO000694A IT1304252B1 (en) | 1998-12-15 | 1998-12-15 | METHOD FOR CLEANING A GUMMER DEVICE. |
| ITBO980694 | 1998-12-15 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1010624A2 true EP1010624A2 (en) | 2000-06-21 |
| EP1010624A3 EP1010624A3 (en) | 2000-07-19 |
Family
ID=11343562
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99124651A Withdrawn EP1010624A3 (en) | 1998-12-15 | 1999-12-10 | Method of cleaning a gumming device |
Country Status (2)
| Country | Link |
|---|---|
| EP (1) | EP1010624A3 (en) |
| IT (1) | IT1304252B1 (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2610192A1 (en) * | 2011-12-30 | 2013-07-03 | Krones AG | Gluing unit |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB263906A (en) * | 1925-09-04 | 1927-01-04 | Martin Feybusch | Improvements in gumming devices particularly suitable for use in labelling machines |
| GB579175A (en) * | 1943-10-13 | 1946-07-25 | Stokes And Smith Co | Improvements in or relating to adhesive-applying apparatus |
| US4369214A (en) * | 1980-05-14 | 1983-01-18 | Jagenberg Werke Ag | Process and apparatus for preventing hardening of glue on inactive bottle labeling machine |
| DE4419578B4 (en) * | 1994-06-03 | 2006-08-31 | Khs Eti-Tec Maschinenbau Gmbh | labeling |
-
1998
- 1998-12-15 IT IT1998BO000694A patent/IT1304252B1/en active
-
1999
- 1999-12-10 EP EP99124651A patent/EP1010624A3/en not_active Withdrawn
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP2610192A1 (en) * | 2011-12-30 | 2013-07-03 | Krones AG | Gluing unit |
Also Published As
| Publication number | Publication date |
|---|---|
| ITBO980694A0 (en) | 1998-12-15 |
| IT1304252B1 (en) | 2001-03-13 |
| ITBO980694A1 (en) | 2000-06-15 |
| EP1010624A3 (en) | 2000-07-19 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP1099634B1 (en) | Spray gumming unit | |
| EP2233018B1 (en) | A gumming device and a method for gumming a web of wrapping material | |
| JPH05508817A (en) | Defoaming/dispensing method and device for sealing/adhesive products | |
| US2991753A (en) | Adhesive applying apparatus | |
| AU724412B2 (en) | Cleaning system for a bag filling machine | |
| CN101466603B (en) | Gluing apparatus | |
| JPS63105763A (en) | Band attaching machine for capsule | |
| US5647411A (en) | Metering method and device | |
| KR20190056796A (en) | Gravure coating device | |
| US3967858A (en) | Cigarette filter rod transfer apparatus | |
| US5170710A (en) | Method and apparatus for handling printing ink | |
| KR101020759B1 (en) | Paper dispenser for selectively carrying liquid-soaked paper or dry paper | |
| JPH09118307A (en) | Device for supplying liquid glue to the glue application mechanism | |
| EP0911085A1 (en) | A spray gumming unit | |
| US3063408A (en) | Tail gluer | |
| US6616763B2 (en) | Dispenser device for dryable fluids | |
| US2368759A (en) | Automatic glue applying machine | |
| ITBO980694A1 (en) | METHOD FOR CLEANING A GUMMER DEVICE. | |
| JP4191880B2 (en) | Liquid ejector | |
| JP2631970B2 (en) | Magnetic card cleaning device | |
| JPH0680127A (en) | Liquid agent supplying device for filling and packing device | |
| JPH0754264Y2 (en) | Glazing device | |
| EP0862951A1 (en) | Gumming device | |
| JPS626860B2 (en) | ||
| EP0787533A1 (en) | Gumming device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE CH CY DE DK ES FI FR GB GR IE IT LI LU MC NL PT SE |
|
| AX | Request for extension of the european patent |
Free format text: AL;LT;LV;MK;RO;SI |
|
| AKX | Designation fees paid | ||
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 20010120 |