EP0774019B1 - Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie - Google Patents
Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie Download PDFInfo
- Publication number
- EP0774019B1 EP0774019B1 EP96920882A EP96920882A EP0774019B1 EP 0774019 B1 EP0774019 B1 EP 0774019B1 EP 96920882 A EP96920882 A EP 96920882A EP 96920882 A EP96920882 A EP 96920882A EP 0774019 B1 EP0774019 B1 EP 0774019B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- approximately
- web
- cylinder
- engraved
- marking
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 36
- 239000000835 fiber Substances 0.000 claims description 31
- 239000000463 material Substances 0.000 claims description 20
- 239000011230 binding agent Substances 0.000 claims description 14
- 238000009826 distribution Methods 0.000 claims description 14
- 239000004753 textile Substances 0.000 claims description 14
- 229910000831 Steel Inorganic materials 0.000 claims description 10
- 239000010959 steel Substances 0.000 claims description 10
- 230000015572 biosynthetic process Effects 0.000 claims description 8
- 229920001169 thermoplastic Polymers 0.000 claims description 8
- 239000004416 thermosoftening plastic Substances 0.000 claims description 8
- 239000004952 Polyamide Substances 0.000 claims description 4
- 229920001971 elastomer Polymers 0.000 claims description 4
- 229920002647 polyamide Polymers 0.000 claims description 4
- 239000005060 rubber Substances 0.000 claims description 4
- 239000012815 thermoplastic material Substances 0.000 claims description 4
- 238000003490 calendering Methods 0.000 claims description 3
- 239000004033 plastic Substances 0.000 claims description 3
- 229920003023 plastic Polymers 0.000 claims description 3
- 239000004814 polyurethane Substances 0.000 claims description 3
- 229920002635 polyurethane Polymers 0.000 claims description 3
- 239000000123 paper Substances 0.000 claims 1
- 230000008569 process Effects 0.000 description 13
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 9
- 230000000875 corresponding effect Effects 0.000 description 7
- 238000012549 training Methods 0.000 description 7
- 238000004049 embossing Methods 0.000 description 5
- 238000004519 manufacturing process Methods 0.000 description 5
- 230000007423 decrease Effects 0.000 description 4
- 230000035882 stress Effects 0.000 description 4
- 230000008901 benefit Effects 0.000 description 3
- 238000004132 cross linking Methods 0.000 description 3
- 230000000694 effects Effects 0.000 description 3
- 239000004744 fabric Substances 0.000 description 3
- 239000003673 groundwater Substances 0.000 description 3
- 239000004816 latex Substances 0.000 description 3
- 229920000126 latex Polymers 0.000 description 3
- 238000005259 measurement Methods 0.000 description 3
- 229920000742 Cotton Polymers 0.000 description 2
- 238000010521 absorption reaction Methods 0.000 description 2
- 238000004458 analytical method Methods 0.000 description 2
- 230000008021 deposition Effects 0.000 description 2
- 238000001035 drying Methods 0.000 description 2
- 238000010438 heat treatment Methods 0.000 description 2
- 239000012943 hotmelt Substances 0.000 description 2
- 230000003287 optical effect Effects 0.000 description 2
- 230000000007 visual effect Effects 0.000 description 2
- 235000015847 Hesperis matronalis Nutrition 0.000 description 1
- 240000004533 Hesperis matronalis Species 0.000 description 1
- 229920001131 Pulp (paper) Polymers 0.000 description 1
- DQXBYHZEEUGOBF-UHFFFAOYSA-N but-3-enoic acid;ethene Chemical compound C=C.OC(=O)CC=C DQXBYHZEEUGOBF-UHFFFAOYSA-N 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 238000004040 coloring Methods 0.000 description 1
- 239000002131 composite material Substances 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 238000007596 consolidation process Methods 0.000 description 1
- 230000002596 correlated effect Effects 0.000 description 1
- 230000003247 decreasing effect Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000001627 detrimental effect Effects 0.000 description 1
- 239000006185 dispersion Substances 0.000 description 1
- 239000000839 emulsion Substances 0.000 description 1
- 239000005038 ethylene vinyl acetate Substances 0.000 description 1
- 230000008642 heat stress Effects 0.000 description 1
- 238000002372 labelling Methods 0.000 description 1
- 238000009304 pastoral farming Methods 0.000 description 1
- 230000035515 penetration Effects 0.000 description 1
- 229920001200 poly(ethylene-vinyl acetate) Polymers 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 230000009467 reduction Effects 0.000 description 1
- 238000010008 shearing Methods 0.000 description 1
- 230000035939 shock Effects 0.000 description 1
- 238000010186 staining Methods 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
- 238000012546 transfer Methods 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
Images
Classifications
-
- D—TEXTILES; PAPER
- D21—PAPER-MAKING; PRODUCTION OF CELLULOSE
- D21F—PAPER-MAKING MACHINES; METHODS OF PRODUCING PAPER THEREON
- D21F11/00—Processes for making continuous lengths of paper, or of cardboard, or of wet web for fibre board production, on paper-making machines
- D21F11/006—Making patterned paper
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/58—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by applying, incorporating or activating chemical or thermoplastic bonding agents, e.g. adhesives
- D04H1/60—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by applying, incorporating or activating chemical or thermoplastic bonding agents, e.g. adhesives the bonding agent being applied in dry state, e.g. thermo-activatable agents in solid or molten state, and heat being applied subsequently
- D04H1/62—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by applying, incorporating or activating chemical or thermoplastic bonding agents, e.g. adhesives the bonding agent being applied in dry state, e.g. thermo-activatable agents in solid or molten state, and heat being applied subsequently at spaced points or locations
-
- D—TEXTILES; PAPER
- D04—BRAIDING; LACE-MAKING; KNITTING; TRIMMINGS; NON-WOVEN FABRICS
- D04H—MAKING TEXTILE FABRICS, e.g. FROM FIBRES OR FILAMENTARY MATERIAL; FABRICS MADE BY SUCH PROCESSES OR APPARATUS, e.g. FELTS, NON-WOVEN FABRICS; COTTON-WOOL; WADDING ; NON-WOVEN FABRICS FROM STAPLE FIBRES, FILAMENTS OR YARNS, BONDED WITH AT LEAST ONE WEB-LIKE MATERIAL DURING THEIR CONSOLIDATION
- D04H1/00—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres
- D04H1/40—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties
- D04H1/58—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by applying, incorporating or activating chemical or thermoplastic bonding agents, e.g. adhesives
- D04H1/64—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by applying, incorporating or activating chemical or thermoplastic bonding agents, e.g. adhesives the bonding agent being applied in wet state, e.g. chemical agents in dispersions or solutions
- D04H1/66—Non-woven fabrics formed wholly or mainly of staple fibres or like relatively short fibres from fleeces or layers composed of fibres without existing or potential cohesive properties by applying, incorporating or activating chemical or thermoplastic bonding agents, e.g. adhesives the bonding agent being applied in wet state, e.g. chemical agents in dispersions or solutions at spaced points or locations
Definitions
- the present invention relates, on the one hand, to a method of finishing a tablecloth formed by the dry route, made up of paper fibers linked by a binder thermoplastic such as latex or hot-melt fibers, and the distribution of fiber is not homogeneous. And, on the other hand, the invention relates to tablecloths as well ennobled.
- the product according to the invention comprising a pattern, is used, after processing, such as tablecloth, napkin or other disposable decorative item.
- This type of sheet is obtained by a well-known process which consists in treating paper pulp in order to dry defibrate them, to form a veil on a canvas formation where the individualized fibers are distributed randomly by air, to bring a thermoplastic binder which will penetrate the veil thus formed allowing fibers to bond together, then dry and crosslink.
- Sheets of cellulosic fibers deposited dry consisting of mattress of randomly distributed paper fibers and a thermoplastic binder, having a pattern on at least one side of the sheet. These tablecloths present on their surface of compressed and other uncompressed areas. Pattern can be obtained by embossing or marking the sheet.
- embossed is understood here to mean creating on a part of a surface of the leaf, reliefs with corresponding depressions on the remaining surface of the leaf. In other words, the sheet which has been embossed has increased in thickness.
- marking as used in the following description consists compressing certain parts on one side of the sheet, forming zones compacted and reducing the thickness of the sheet in these areas without forming relief on the opposite side.
- the compressed or marked parts have a higher density important than the parts that have not been compressed. Unmarked areas may or may not be calendared.
- marking the tablecloth deposited in the dry state was used to improve applying the binder to the sheet.
- part of the sheet surface is compressed by cylindrical rollers before the binding step, the pattern then being stabilized with the binder.
- marking the web is a step inside the method of manufacturing the web.
- the dry-laid fibrous web is marked to increase its bulk and improve its absorption properties. At least 40 percent and preferably between 50 and 80 percent of the total area of one side of the sheet is marked. Both sides can be marked.
- the method consists in marking the dry-laid sheet with a hollow pattern by means of cylindrical rollers which, preferably, are not resilient, these rollers being heated between 140 and 180 ° C and exerting sufficient pressure to densify the parts of the tablecloth located under the compressed areas and reach a density of between approximately 0.2 g / cm 3 and approximately 0.5 g / cm 3 .
- the marking step is carried out here at any time after the deposition of the dry fibers on a mobile support and the consolidation of the sheet.
- this type of product whose absorption properties have been improved, has strength properties, in particular breaking strength, which tend to decrease due to shearing of the fibers. Surface properties such as touch, softness are altered. Indeed, the marking process used for this type of product and the size of the marked area, i.e., areas compacted, are probably at the origin of the decrease in these properties. The product is less soft and less comfortable to use, which is detrimental in some applications such as napkins.
- the sheets have an uneven distribution of their fibers. Some parts of the tablecloth show clumps of fiber while other parts have clear areas with much less fiber.
- a marking by means of a cylinder engraved in steel and a receiving cylinder also made of steel, it can be seen that the zones of high grammage, "overweight", are well marked while the areas of low grammage is not or only slightly marked.
- the areas of high grammage form "wedges" between which the marking is weak. Onne cannot distribute pressure evenly across the generator. The marking is therefore not regular.
- the tablecloth thus marked does not have a pattern uniform and is of lower quality from an aesthetic point of view. This defect appears for sheets of fibers deposited dry, which in particular have a dispersion of weight of plus or minus 20 percent.
- US Patent No. 4,476,078 discusses this problem in the case where the step of marking occurs after drying and crosslinking of the web. Indeed, it does note that with this process, we cannot have a good definition of the marking, nor a high quality at the level of the imprint of the motif. It offers as a solution process consisting in partially crosslinking the binder after its application on the web, to obtain a partially crosslinked and deformable sheet which can keep a physical clothing during transport to the marking station and during marking proper, marking the partially crosslinked sheet and finally completely crosslink the marked sheet.
- Such a method has drawbacks: the marking must be done at the place of crosslinking, therefore probably on the place of manufacture of the tablecloth itself and the process itself is longer and more complex.
- the object of the invention is to overcome all the drawbacks mentioned previously by providing a process of finishing the tablecloth which is a simple groundwater transformation process, economical and flexible in the measurement where the engraved cylinder can be easily changed allowing to modify the pattern marked on the tablecloth.
- Another object of the invention is to provide a marked tablecloth whose pattern is regular whatever the distribution of the fibers in the sheet, while maintaining the mechanical properties of the water table and its surface properties.
- the properties of resistance of the water table are little modified.
- the distortion imparted by the engraving is permanent which constitutes an undeniable advantage.
- effects matt and shiny are given so that the tablecloth can present plays of light coming from the opposition of hollows and reliefs.
- the hollow part, corresponding to the compressed part gives shine.
- the thickness of the web decreases or not, compared to its initial thickness.
- the invention relates to a particular method of marking a tablecloth formed by the dry route, made up of paper fibers linked by a binder thermoplastic such as latex or thermoplastic fibers, and the distribution of which fiber is not perfectly homogeneous, using a marking technique known in the field of textiles to ennoble fabrics; it is the embossing of fabrics.
- the method consists in deform under hot stress the web between a hard engraved cylinder and not deformable and a receiving cylinder with a hardness between about 60 and about 90 degrees Shore D, resilient and deformable under the pressure exerted by said cylinder serious.
- the resilience of the receiving cylinder is defined here by the ratio between the energy restored by the cylinder after deformation and the energy which had been supplied to it for the deform. This ratio can be determined from the hysteresis cycles obtained by successive traction and release using a dynamometer or by submitting a test tube to a shock thanks to a pendulum.
- the receiving cylinder is produced in a material which can undergo deformations, such as a paper material, rubber, polyamide, polyurethane or even textiles.
- the engraved cylinder is in steel and is heated to a temperature ranging from about 80 to about 180 ° C and preferably about 130 to about 150 ° C.
- the subject of the invention is also a sheet formed by the dry process, consisting of paper fibers linked by a thermoplastic material, the fiber distribution is not perfectly homogeneous, with an index of training of less than about 75 measured on a KAJAANI apparatus in the raw state, and comprising on at least one of its faces a marked pattern.
- the rate of marking of the area of the tablecloth having the marked pattern is greater than about 80 percent.
- the surface marked groundwater is less than 40 percent of the total area.
- the subject of the invention is also a sheet obtained according to the method according to the invention, characterized by its marked area, which is greater than 40 percent of the total surface.
- the problem posed in the present invention comes from the fact that the sheet intended to be ennobled is made up of bonded paper fibers which are not distributed uniform or homogeneous in the tablecloth. Indeed, the density varies inside of the same tablecloth to a greater or lesser extent.
- the distribution of the fibers in the sheet will be described below, before marking and before staining, by the epair or formation index which is an index measuring the regularity of the arrangement of the fibers in the thickness of the sheet.
- the visual aspect of the product seen through transparency gives a qualitative measure of the air.
- the index of training can be quantitatively measured by optical means.
- the training index in the following way: we pass light through the sheet and the intensity of the light transmitted through this sheet is measured. This measurement is performed on a suitable device, here a training analyzer marketed under the name KAJAANI, a fully automated optical device.
- the uniformity or regularity of the distribution of the fibers is determined by measuring the variation in the intensity of the light transmitted through a sample. The surface of the sample measured is 63.5 millimeters by 63.5 millimeters.
- the analyzer picks up the sample image, divides it into pixels and stores it in memory. Each pixel is then resolved in 256 discrete levels of gray.
- the computer calculates so statistics a histogram and the formation index of the measured sample.
- the index of training varies in a scale from 20 to 122, 4; a high value corresponds to a better training, more uniform. The most uniform formation (measured without sample) is 122.4.
- the measurement of the formation index is carried out on sheets in the raw state, ie white tablecloths corresponding to the tablecloths before coloring and before marking.
- the sheets used in the process according to the invention have an index of training below about 75.
- a well-formed sheet can have a grammage variation of ⁇ 4 grams.
- the binder is essentially latex and in general, an emulsion of ethylene-vinyl-acetate type, or even powders or hot-melt fibers.
- these layers are already linked, that is to say consolidated by the binder. thermoplastic, dried and crosslinked.
- the method according to the invention takes place in outside the manufacturing process of the sheet itself or at the end of the latter, unlike most prior art methods where the marking step takes place after the deposition of the dry fibers and before the tying operation has been completed.
- the method according to the invention consists in deforming under heat stress the tablecloth to permanently mark a decorative motif on at least one of its faces.
- the stress deformation step and the heating step can be simultaneous or dissociated according to the nature of the engraved cylinder.
- the latter is made of a hard, non-deformable material.
- this cylinder is engraved steel.
- the steel cylinder is directly heated.
- the heating step would be dissociated from that of compression as has already been proposed for the embossing of textiles.
- the pattern is engraved on the hard, non-deformable cylinder.
- the cylinder surface is more or less engraved depending on the type of tablecloth desired.
- the pattern engraved on the surface of the cylinder has raised parts which correspond to the parts marked in hollow on the surface of the tablecloth.
- a maximum of 40 percent of the surface of the cylinder is etched and preferably between about 10 and about 40 percent and again more preferably between about 15 and about 30 percent.
- the engraving pattern in this case, is quite decorative.
- the drawing can, for example, consist of several unitary patterns such as a flower or other, or thickened lines or lines giving a marbled effect etc.
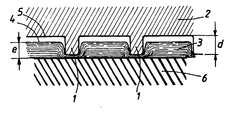
- the height d of part 1 in relief on the cylinder engraved 2 or the depth of the engraving must be strictly greater than the thickness e of the sheet or of the sheet 3 which is intended to be marked so that the surface 4 of the sheet which is not marked, that is to say which is not deformed by the part 1 in relief of the engraved cylinder 2, is not in contact with part 5 without relief of the engraved cylinder 2 which, moreover, is heated in the general case. Because of this, the thickness of the initial water table is not changed significantly.
- a second type of tablecloth For a second type of tablecloth, more than 40 percent and preferably between 60 and 90 percent of the cylinder surface is etched. The pattern is then much more small and can be in the form of multiple points. In the latter case, the marking gives an overall aspect of the textile weft to the tablecloth. Indeed, for this type of tablecloth, we are looking for a textile look and feel of the finished textile type such as starched cotton, that is to say a hand print of fabrics. We also aim to obtain a sheet of constant thickness and less than the initial thickness, always in the spirit of having a product of textile appearance or imitation.
- the depth of the engraving is, for the second type of sheet, less than the thickness of the sheet. Therefore, with in plus a large marked surface, the sheet decreases substantially in thickness.
- the receiving cylinder also known as a counter-cylinder is produced in a resilient or "elastic" material, as defined above, and may be subject to deformations when the engraved cylinder exerts stresses.
- the material used for this receiving cylinder should have a hardness in the range of about 60 to about 90 degrees Shore D.
- the hardness of this material will be in the range from from about 65 to about 85 degrees Shore D.
- the material used are: rubber having for example a hardness of about 88 degrees Shore D for the rubber marketed under the Polylay brand, paper having for example a hardness of about 78 to about 82 degrees Shore D, the polyamide having a hardness about 80 degrees Shore D or a textile material having a hardness of about 78 at about 85 degrees Shore D.
- the cylinder of textile material gives good results.
- a cylinder of "composite" material where the heart of the cylinder is made of paper and the cylinder covering is made of textile material for example woolly type. The hardness of such a cylinder is about 82 degrees Shore D.
- the polyamide is also very suitable allowing a good distribution of the effort over the entire surface of the cylinder and matching the surface of the patterns. Any material equivalent elastic plastic can be considered.
- a counter cylinder made of special quality polyurethane with a hardness of approximately 75 degrees Shore D.
- the receiving cylinder or counter-cylinder is flexible and admits irregularities of thickness of the tablecloth. It deforms advantageously along the contour of the parts protruding from the engraved cylinder when the latter is applied under pressure and at hot on the tablecloth intended to be marked.
- the sheet is hot stamped between the engraved steel cylinder which is heated, and the cylinder receiver or counter-cylinder.
- the engraved cylinder is heated to a temperature equivalent to the softening or creep temperature of the material constituting the tablecloth in the compressed area, i.e. at a temperature between about 80 and 180 ° C and preferably between about 130 and 150 ° C.
- the engraved cylinder exerts a linear pressure on the sheet, which can vary in a range from about 40 to about 150 kg / cm and preferably about 60 to about 100 kg / cm.
- the machine may have a speed of about 10 to about 300 m / min. and preferably about 80 to 200 m / min. It should be noted that the temperature increases with speed of the machine. As we are looking for a permanent effort, for a speed of scrolling or a given machine speed, pressure and temperature of the engraved cylinder should be correlated. Preferably, only one side of the web is marked but both sides can be marked.
- the tablecloth resulting from this process is marked.
- the marked areas are compacted and their density has increased.
- the grammage of the marked web varies little compared to that of the initial tablecloth.
- the marked pattern is very regular and permanent.
- the marked surface of the tablecloth is less than 40 percent of the total area of the water table, unlike the water table marked with means of the method described in European patent No. 0 077 055 of the prior art.
- this marked area varies in the range of from about 15 to about 30 percent of the total area of the water table. This limitation of the marked area is essential for this type of tablecloth.
- the average thickness of the web as well marked decreased very little in the range of 0.02 to 0.2 mm and preferably less than 0.1 mm from the initial thickness.
- the web advantageously keeps the surface properties before marking, such as its soft feel and its softness.
- the tablecloth thus marked presents a greater softness than tablecloths marked with classic way.
- This characteristic can be quantified by measuring the marking rate of the tablecloth.
- the marking rate corresponds to the efficiency of the image transfer from the engraving of the cylinder engraved on the tablecloth.
- This labeling rate was measured by analysis image on a device marketed under the name Quantimet 600 by the company LEICA.
- the method of analysis consists in subjecting groundwater samples to a grazing lighting at a certain angle, thus highlighting the relief of the pattern in creating gray areas.
- the area of the shaded areas is measured from a threshold of gray determined from a witness.
- the marking rate is the following ratio: marked surface of the water table (by relative to the total surface of the water table) on the theoretical marked surface (corresponding to the engraved surface of the cylinder) relative to the total surface of the web.
- a marking rate of 0 percent corresponds to an area that has not been marked and a marking rate of 100 percent corresponds to an ideal marking or perfect.
- the 100 percent marking rate is in fact the perfect imprint of the relief of the engraved cylinder.
- the tablecloth marked according to the invention corresponding to the first type of tablecloth, i.e. at the tablecloth whose marked surface is less than 40 percent, present a marking rate greater than about 80 percent and preferably greater than 90 percent.
- Another advantageous characteristic of the first type of sheet is that it has shiny surface portions alternating with surface portions matt, clearly visible to the naked eye, the shiny parts corresponding to the marked surface of the tablecloth. This matt and shiny effect brings out the motif clearly and contributes to the refinement of the tablecloth. It gives a satin appearance to the marked surface part and reminds, in terms of touch and appearance, damask cotton.
- the marked area is more than 40 percent of the total surface of the water table.
- the tablecloth has a smaller apparent thickness compared to its initial thickness. The reduction in thickness is around 25 percent of the initial thickness.
- This tablecloth also has the advantage of having a constant thickness which is not always the case with the initial ply at the end of its manufacture.
- the rigidity can be advantageously increased so that, for example, napkins can have a finished textile feel and, when folded for presentation, keep this shape folded. To do this, we increase the grammage of the tablecloth and we choose an appropriate binder.
- the tablecloth marked according to the invention whatever its marked surface, has mechanical properties, in particular resistance properties, substantially identical to those of the sheet before treatment.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Dispersion Chemistry (AREA)
- General Chemical & Material Sciences (AREA)
- Treatment Of Fiber Materials (AREA)
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
- Nonwoven Fabrics (AREA)
- Paper (AREA)
- Laminated Bodies (AREA)
Description
- la figure unique représente une vue partielle d'une nappe comprimée entre un cylindre gravé en acier et un cylindre récepteur résilient et déformable, la nappe correspondant au premier type de nappe décrit ci-après.
Claims (19)
- Procédé d'ennoblissement d'une nappe formée par voie sèche, constituée de fibres papetières liées par un liant thermoplastique, et dont la répartition des fibres n'est pas parfaitement homogène, caractérisée en ce qu'il consiste à déformer sous contrainte à chaud et à marquer de manière permanente ladite nappe entre un cylindre gravé dur et non déformable et un cylindre récepteur d'une dureté comprise entre environ 60 et environ 90 degrés Shore D, résilient et déformable sous la pression exercée par ledit cylindre gravé.
- Procédé selon la revendication précédente, caractérisé en ce que ledit cylindre récepteur a une dureté de préférence d'environ 65 à environ 85 degrés Shore D.
- Procédé selon la revendication 1 ou 2, caractérisé en ce que le cylindre récepteur est réalisé dans un matériau qui peut subir des déformations, tel qu'un matériau papier, caoutchouc, polyamide, polyuréthane ou encore textile.
- Procédé selon l'une des revendications précédentes, caractérisé en ce que le cylindre gravé dur est réalisé en acier ou tout matériau qui ne se déforme pas sous la pression exercée, tel que par exemple un matériau plastique.
- Procédé selon la revendication 4, caractérisé en ce que le cylindre gravé est en acier et est chauffé à une température allant d'environ 80 à environ 180° C et de préférence d'environ 130 à environ 150° C.
- Procédé selon l'une des revendications précédentes, caractérisé en ce que la pression linéaire du cylindre gravé est d'environ 40 à environ 150 kg/cm et de préférence d'environ 60 à environ 100 kg/cm.
- Procédé selon l'une des revendications précédentes, caractérisé en ce qu'on effectue un calandrage simultanément au marquage.
- Procédé selon l'une des revendications 1 à 6, caractérisé en ce qu'environ 10 à environ 40 pour cent de la surface du cylindre dur et non déformable est gravée.
- Procédé selon la revendication 8, caractérisé en ce qu'environ 15 à environ 30 pour cent de la surface dudit cylindre est de préférence gravée.
- Procédé selon la revendication 8 ou 9, caractérisé en ce que la profondeur de la gravure est supérieure à l'épaisseur de la nappe.
- Nappe formée par voie sèche, constituée de fibres papetières liées par une matière thermoplastique, dont la répartition des fibres n'est pas parfaitement homogène, présentant un indice de formation inférieur à 75 mesuré sur un appareil KAAJANI à l'état brut et comportant sur au moins une de ses faces un motif, caractérisée en ce que le motif a été obtenu par marquage à chaud entre un cylindre gravé dur et non déformable et un cylindre récepteur d'une dureté comprise entre environ 60 et environ 90 degrés Shore D, résilient et déformable sous la pression exercée par ledit cylindre gravé, et en ce que sur la partie de la surface de la nappe comportant ledit motif le taux de marquage est supérieur à environ 80 pour cent.
- Nappe selon la revendication 11, caractérisée en ce que ledit taux de marquage est de préférence supérieur à 90 pour cent.
- Nappe selon la revendication 11 ou 12, caractérisée en ce que la surface marquée de ladite nappe est inférieure à 40 pour cent de la surface totale.
- Nappe selon la revendication 13, caractérisée en ce que la surface marquée de la dite nappe est de préférence comprise entre environ 15 et environ 30 pour cent de la surface totale de ladite nappe.
- Nappe selon l'une des revendications 11 à 14, caractérisée en ce la surface de la nappe comportant ledit motif présente des parties de surface brillantes alternant avec des parties de surface mates, lesdites parties de surface brillantes correspondant à la surface marquée.
- Nappe selon l'une des revendications 11 à 15, caractérisée en ce qu'elle a une épais d'environ 0,5 à environ 1 mm.
- Nappe formée par voie sèche, constituée de fibres papetières liées par une matière thermoplastique, dont la répartition des fibres n'est pas parfaitement homogène et comportant sur au moins une de ses faces un motif, caractérisée en ce que le motif a été obtenu par marquage à chaud entre un cylindre gravé dur et non déformable et un cylindre récepteur d'une dureté comprise entre environ 60 et environ 90 degrés Shore D, résilient et déformable sous la pression exercée par ledit cylindre gravé et en ce que la surface marquée de ladite nappe est supérieure à 40 pour cent de la surface totale de la nappe.
- Nappe selon l'une des revendications 11 à 17, caractérisée en ce qu'elle a un grammage compris entre environ 50 et environ 120 g/m2.
- Nappe selon l'une des revendications 11 à 18, caractérisée en ce que la nappe contient entre environ 10 et environ 50 pour cent en poids de matière thermoplastique.
Priority Applications (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP96920882A EP0774019B1 (fr) | 1995-06-01 | 1996-05-31 | Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie |
| GR990402582T GR3031489T3 (en) | 1995-06-01 | 1999-10-08 | Method for finishing a dry-laid web and web finished thereby |
Applications Claiming Priority (5)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP95401288A EP0745717A1 (fr) | 1995-06-01 | 1995-06-01 | Procédé d'ennoblissement d'une nappe formée par voie sèche et nappe ainsi ennoblie |
| EP95401288 | 1995-06-01 | ||
| EP96920882A EP0774019B1 (fr) | 1995-06-01 | 1996-05-31 | Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie |
| PCT/FR1996/000825 WO1996038618A1 (fr) | 1995-06-01 | 1996-05-31 | Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie |
| US08/756,527 US5858512A (en) | 1995-06-01 | 1996-11-26 | Air-laid web formed from a finishing process and web obtained thereby |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0774019A1 EP0774019A1 (fr) | 1997-05-21 |
| EP0774019B1 true EP0774019B1 (fr) | 1999-07-21 |
Family
ID=26140555
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95401288A Withdrawn EP0745717A1 (fr) | 1995-06-01 | 1995-06-01 | Procédé d'ennoblissement d'une nappe formée par voie sèche et nappe ainsi ennoblie |
| EP96920882A Expired - Lifetime EP0774019B1 (fr) | 1995-06-01 | 1996-05-31 | Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP95401288A Withdrawn EP0745717A1 (fr) | 1995-06-01 | 1995-06-01 | Procédé d'ennoblissement d'une nappe formée par voie sèche et nappe ainsi ennoblie |
Country Status (7)
| Country | Link |
|---|---|
| EP (2) | EP0745717A1 (fr) |
| DE (1) | DE69603342T2 (fr) |
| DK (1) | DK0774019T3 (fr) |
| ES (1) | ES2136422T3 (fr) |
| GR (1) | GR3031489T3 (fr) |
| NO (1) | NO308012B1 (fr) |
| WO (1) | WO1996038618A1 (fr) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6090241A (en) * | 1997-06-06 | 2000-07-18 | The Procter & Gamble Company | Ultrasonically-assisted process for making differential density cellulosic structure containing fluid-latent indigenous polymers |
| US6139686A (en) * | 1997-06-06 | 2000-10-31 | The Procter & Gamble Company | Process and apparatus for making foreshortened cellulsic structure |
| US5938893A (en) * | 1997-08-15 | 1999-08-17 | The Procter & Gamble Company | Fibrous structure and process for making same |
| US5935381A (en) * | 1997-06-06 | 1999-08-10 | The Procter & Gamble Company | Differential density cellulosic structure and process for making same |
Family Cites Families (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4127637A (en) | 1975-03-13 | 1978-11-28 | Scott Paper Co. | Method of manufacturing a dry-formed, embossed adhesively bonded, nonwoven fibrous sheet |
| US4135024A (en) | 1976-08-16 | 1979-01-16 | Scott Paper Company | Method of treating a low integrity dry-formed nonwoven web and product made therefrom |
| US4507173A (en) * | 1980-08-29 | 1985-03-26 | James River-Norwalk, Inc. | Pattern bonding and creping of fibrous products |
| CA1193919A (fr) | 1981-10-05 | 1985-09-24 | Michael P. Bouchette | Tissu fibreux forme a sec ayant des caracteristiques superieures d'absorption |
| US4476078A (en) | 1982-05-04 | 1984-10-09 | James River-Dixie/Northern, Inc. | Process for manufacturing embossed nonwoven fibrous products |
-
1995
- 1995-06-01 EP EP95401288A patent/EP0745717A1/fr not_active Withdrawn
-
1996
- 1996-05-31 ES ES96920882T patent/ES2136422T3/es not_active Expired - Lifetime
- 1996-05-31 DK DK96920882T patent/DK0774019T3/da active
- 1996-05-31 EP EP96920882A patent/EP0774019B1/fr not_active Expired - Lifetime
- 1996-05-31 WO PCT/FR1996/000825 patent/WO1996038618A1/fr not_active Ceased
- 1996-05-31 DE DE69603342T patent/DE69603342T2/de not_active Expired - Lifetime
-
1997
- 1997-01-30 NO NO970401A patent/NO308012B1/no unknown
-
1999
- 1999-10-08 GR GR990402582T patent/GR3031489T3/el unknown
Also Published As
| Publication number | Publication date |
|---|---|
| DE69603342D1 (de) | 1999-08-26 |
| NO970401D0 (no) | 1997-01-30 |
| NO308012B1 (no) | 2000-07-03 |
| GR3031489T3 (en) | 2000-01-31 |
| EP0745717A1 (fr) | 1996-12-04 |
| DK0774019T3 (da) | 1999-11-29 |
| EP0774019A1 (fr) | 1997-05-21 |
| ES2136422T3 (es) | 1999-11-16 |
| NO970401L (no) | 1997-03-18 |
| DE69603342T2 (de) | 1999-11-11 |
| WO1996038618A1 (fr) | 1996-12-05 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2039815B1 (fr) | Article de nettoyage et/ou de soin de la peau comportant un motif en relief à sa surface et procédé de fabrication dudit article | |
| EP1189531B1 (fr) | Produit de coton hydrophile comportant une face douce et une face grattante | |
| EP0864014B1 (fr) | Tissu-papier marque d'une empreinte simulant un filigrane et procede de fabrication associe | |
| FR2735155A1 (fr) | Produit en papier absorbant mince doux et souple, et son procede de fabrication | |
| FR2991345A1 (fr) | Structures fibreuses et leurs procedes de preparation | |
| FR2604734A1 (fr) | Feuille stratifiee absorbante | |
| FR2814476A1 (fr) | Feuille de securite comportant une couche transparente ou translucide | |
| FR2715052A1 (fr) | Produit cellulosique à jets multiples à résistance accrue à l'état humide. | |
| FR2983494A1 (fr) | Structures fibreuses et procedes de production de celles-ci | |
| FR2768443A1 (fr) | Papier couche comportant une marque ressemblant a un filigrane et procede de fabrication | |
| EP2914776B1 (fr) | Papier decoratif pour stratifies | |
| EP2576904A1 (fr) | Papier fin couché à toucher doux | |
| US6041701A (en) | Process of finishing an air-laid web and web obtained thereby | |
| JP6947358B2 (ja) | 基板へのセキュリティデバイスの表面貼付の方法 | |
| US5858512A (en) | Air-laid web formed from a finishing process and web obtained thereby | |
| CA2428583C (fr) | Procede de marquage d'une feuille de papier, feuille ayant un motif de type filigrane | |
| FR2672311A1 (fr) | Feuille de non-tisse a plusieurs couches non emboitantes et procede de fabrication. | |
| EP0774019A1 (fr) | Procede d'ennoblissement d'une nappe formee par voie seche et nappe ainsi ennoblie | |
| WO2018141915A1 (fr) | Papier decor pour stratifies | |
| FR2562918A1 (fr) | Procede pour fabriquer un article textile en nappe floque, et article textile en nappe floque souple obtenu par la mise en oeuvre du procede | |
| WO2004003294A2 (fr) | Procede de fabrication d'une feuille portant un motif en relief | |
| CA2099871C (fr) | Feuille imprimable marquee couchee et son procede de fabrication | |
| WO2008049811A1 (fr) | Procédé de traitement pour base d'impression de papier mélamine | |
| CA2202166C (fr) | Papier absorbant gaufre a motifs combines | |
| CA2318384A1 (fr) | Utilisation d'une feuille papetiere permeable a l'air comme element support d'un empilement d'etoffes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE CH DE DK ES FI FR GB GR IE IT LI NL PT SE |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: LESAGE, HENRI Inventor name: LOUIS DIT PICARD, BERNARD Inventor name: NEVEU, JEAN-LOUIS |
|
| 17P | Request for examination filed |
Effective date: 19970605 |
|
| 17Q | First examination report despatched |
Effective date: 19971118 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: FORT JAMES FRANCE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE CH DE DK ES FI FR GB GR IE IT LI NL PT SE |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: NV Representative=s name: MICHELI & CIE INGENIEURS-CONSEILS |
|
| REF | Corresponds to: |
Ref document number: 69603342 Country of ref document: DE Date of ref document: 19990826 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19990817 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19991021 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2136422 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: CD |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20040422 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20040426 Year of fee payment: 9 Ref country code: DK Payment date: 20040426 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20040427 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20040428 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GR Payment date: 20040429 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050506 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050601 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20051205 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| EUG | Se: european patent has lapsed | ||
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20140425 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20140529 Year of fee payment: 19 Ref country code: NL Payment date: 20140423 Year of fee payment: 19 Ref country code: IT Payment date: 20140428 Year of fee payment: 19 Ref country code: DE Payment date: 20140424 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20140423 Year of fee payment: 19 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20140521 Year of fee payment: 19 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69603342 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20150531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150531 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20150601 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20160129 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150601 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20151201 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150601 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20160627 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150601 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150531 |