EP0748877B1 - Procédé de réalisation d'une bande de tôle d'acier laminée à chaud à très haute limite d'élasticité et tôle d'acier obtenue - Google Patents
Procédé de réalisation d'une bande de tôle d'acier laminée à chaud à très haute limite d'élasticité et tôle d'acier obtenue Download PDFInfo
- Publication number
- EP0748877B1 EP0748877B1 EP96401263A EP96401263A EP0748877B1 EP 0748877 B1 EP0748877 B1 EP 0748877B1 EP 96401263 A EP96401263 A EP 96401263A EP 96401263 A EP96401263 A EP 96401263A EP 0748877 B1 EP0748877 B1 EP 0748877B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- sheet
- steel sheet
- niobium
- temperature
- thickness
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/14—Ferrous alloys, e.g. steel alloys containing titanium or zirconium
Definitions
- the invention relates to a method for producing a sheet metal strip. hot rolled steel with very high yield strength, particularly for the shaping of parts and having a brittle / ductile transition to a temperature below -50 ° C.
- Controlled rolling keeps sheet steel in a low equivalent carbon level and obtain mechanical properties wanted by refining of the ferritic structure grain and coherent precipitation niobium carbonitride, niobium can be combined with titanium or vanadium.
- a product such as a ULCB steel sheet (bainitic structure low carbon) has a higher yield strength at 700 MPa and a brittle / ductile transition temperature of approximately - 60 ° C.
- flawless 180 ° bending of the steel sheet is limited to internal bending diameters greater than 2.5 times the thickness of the sheet in the rolling direction and greater than 3 times the thickness of the sheet in the cross direction of rolling.
- a product such as a micro-alloy steel sheet has a yield strength greater than 700 MPa and can be bent 180 ° without generating a defect for a bending diameter less than twice the thickness of the sheet but this steel has the disadvantage of having a temperature of ductile / brittle transition between -20 ° C and -40 ° C.
- the object of the invention is to present a method for producing a strip of hot-rolled steel sheet with very high yield strength especially for the shaping of parts and presenting a possibility faultless 180 ° bending under a bending diameter of less than twice sheet thickness and brittle / ductile transition at a lower temperature at -50 ° C.
- the invention also relates to a steel sheet as defined in claim 4.
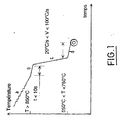
- Figure 1 is a curve showing schematic, according to the method of the invention, the variation of temperature as a function of time, imposed on the strip of hot-rolled sheet steel.
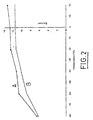
- Figure 2 shows transition curves brittle / ductile for a 5 mm thick steel sheet, brittle / ductile transition measured in the direction long and crosswise of the rolled sheet strip hot.
- the basic composition provides a ferrite microstructure and hardened granular bainite by precipitation of niobium-titanium microalloy elements.
- the rolling process according to the invention aims to obtain a good recrystallization of the austenitic grains at the exit of the rolling mill stands thus allowing obtaining an equiaxed structure.
- Steel structure of sheet metal strip allows high elongations greater than 15 % up to 20% and bending at 180 ° without defect with smaller inside bending diameters twice the thickness of the sheet.
- the temperature at the end of rolling is greater than 850 ° C, and preferably 900 ° C in order to limit the precipitation of micro-alloying elements induced by hot rolling and secondly, to make the most of their effect hardening during controlled cooling.
- Controlled cooling is imposed on the belt hot-rolled sheet after a time interval less than 10 seconds between the end of hot rolling and the start of controlled cooling.
- the time interval is of the order of 1.5 seconds, this which ensures a very fine grain size and a limit high elasticity.
- the controlled cooling rates are chosen between 20 ° C per second and 100 ° C per second in depending on the thickness of the sheet strip to be treated.
- the controlled cooling rate is, on average 40 ° C per second for a strip of sheet metal about 5 mm thick. Under these conditions, there are hardening precipitation of microalloy elements, which provides an upper yield strength at 700 MPa, or 740 MPa.
- End of controlled cooling temperature is between 550 ° C and 750 ° C and preferably 650 ° C, which ensures hardening precipitation of microalloy elements.
- Figure 1 is a diagrammatic curve, according to the process of the invention, the temperature variation in time function imposed on the sheet steel strip after hot rolling. After rolling to a temperature greater than 850 ° C represented by the portion of curve "a”, a period of less than 10 seconds, represented by the portion of curve "b", is requested before controlled cooling of the rolled sheet strip hot which is represented by the portion of curve "c".
- Figure 2 shows two transition curves A and B brittle / ductile, i.e. curves giving the breaking energy of a test piece taken from a sheet metal as a function of temperature.
- Curves A and B relate to a steel sheet 5 mm thick and the brittle / ductile transition is measured respectively in the long direction and in the cross direction of the sheet hot rolled.
- the sheet steel strip according to the invention does not have a brittle / ductile transition in the temperature range between + 20 ° C and -80 ° C. All the ruptures are therefore ductile up to -80 ° C.
- the brittle / ductile transition temperature is therefore less than -80 ° C.
- the method according to the invention allows the realization thick hot-rolled steel sheet between 2.5 and 10 mm, sheet of which the steel has an elastic limit greater than 700 MPa.
- Prison steel can be subjected to a 180 ° bend without defects, the inside diameter of the folding can be less than twice the thickness of the sheet.
- Titanium participates in precipitation hardening in the form of TiC.
- Molybdenum allows after precipitation microalloy elements in the form of carbide, limit carbon diffusion at high temperatures thus ensuring obtaining fine precipitates in the ferritic matrix and lowering the temperature of fragile / ductile transition at a temperature always located below -50 ° C in the case of a steel according to the composition defining the invention.
- the hot-rolled sheet strip according to the invention can be used for parts manufacturing folded profiled or stamped with reduced thickness for their lightening and / or pieces having better mechanical characteristics in fatigue.
- the low temperature of brittle / ductile transition offers the possibility operation of pieces of equipment, entering through example in the construction of cranes, in a field of very low temperature without risk of fragile breakage.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Heat Treatment Of Sheet Steel (AREA)
- Heat Treatment Of Steel (AREA)
- Heat Treatment Of Strip Materials And Filament Materials (AREA)
Description
- carbone ≤ 0,1%,
- 1 % ≤ manganèse ≤ 1,5 %
- silicium ≤ 0,3 %
- phosphore ≤ 0,03 %,
- soufre ≤ 0,01 %,
- 0,01 % ≤ aluminium ≤ 0,1 %,
- 0,04 % ≤ niobium ≤ 0,06 %,
- 0,1 % ≤ titane ≤ 0,15%,
- 0,1 %≤ molybdène ≤ 0,2 %,
est, après laminage à chaud, soumis à un refroidissement contrôlé à une vitesse de refroidissement comprise entre 20°C par seconde et 100°C par seconde jusqu'à une température de fin de refroidissement comprise entre 550°C et 750°C, de façon à obtenir une microstructure de ferrite et bainite granulaire durcie par la précipitation des éléments de micro-alliage niobium-titane.
- la température de fin de laminage à chaud est de préférence supérieure à 850°C ou même 900°C ;
- le temps séparant la fin du laminage à chaud et le début du refroidissement contrôlé est de préférence inférieur à 10 secondes et par exemple de l'ordre de 1,5 seconde.
- carbone ≤ 0,1 %,
- 1 % ≤ manganèse ≤ 1,5 %,
- silicium ≤ 0,3 %,
- phosphore ≤ 0,03 %,
- soufre ≤ 0,01 %,
- 0,01 % ≤ aluminium ≤ 0,1 %,
- 0,04 % ≤ niobium ≤ 0,06 %,
- 0,1 % ≤ titane ≤ 0,15 %,
- 0,1 % ≤ molybdène ≤ 0,2 %.
- 0,06 % ≤ carbone ≤ 0,08 %,
- 1,4 % ≤ manganèse ≤ 1,5 %,
- 0,2 % ≤ silicium ≤ 0.26 %,
- phosphore ≤ 0,02 %,
- soufre ≤ 0,005 %,
- 0,02 % ≤ aluminium ≤ 0,06 %,
- 0,055 % ≤ niobium ≤ 0,06 %,
- 0,110 % ≤ titane ≤ 0,14 %,
- 0,130 % ≤ molybdène ≤ 0,170 %.
Claims (4)
- Procédé de réalisation d'une bande de tôle d'acier laminée à chaud d'épaisseur comprise entre 2,5 mm et 10 mm, dont la limite d'élasticité est supérieure à 700 MPa et qui peut être pliée à 180° sans défaut sous un diamètre intérieur de pliage inférieur à deux fois l'épaisseur de la tôle, utilisable notamment pour la mise en forme de pièces et présentant une transition fragile/ductile à une température inférieure à -50°C, caractérisé en ce que l'acier de composition pondérale suivante :le reste, à l'exception des impuretés inhérentes à la fabrication, étant constitué par du fer,carbone ≤ 0,1%,1 % ≤ manganèse ≤ 1,5 %silicium ≤ 0,3 %phosphore ≤ 0,03 %,soufre ≤ 0,01 %,0,01 % ≤ aluminium ≤ 0,1 %,0,04 % ≤ niobium ≤ 0,06 %,0,1 % ≤ titane ≤ 0,15%,0,1 %≤ molybdène ≤ 0,2 %,
est, après laminage à chaud, soumis à un refroidissement contrôlé à une vitesse de refroidissement comprise entre 20°C par seconde et 100°C par seconde jusqu'à une température de fin de refroidissement comprise entre 550°C et 750°C, de façon à obtenir une microstructure de ferrite et bainite granulaire durcie par la précipitation des éléments de micro-alliage niobium-titane. - Procédé selon la revendication 1, caractérisé en ce que la température de fin de laminage à chaud est supérieure à 850°C.
- Procédé selon les revendications 1 e 2, caractérisé en ce que le temps séparant la fin du laminage à chaud et le début du refroidissement contrôlé est inférieur à 10 secondes.
- Tôle d'acier laminée à chaud d'une épaisseur comprise entre 2,5 mm et 10 mm ayant une limite d'élasticité supérieure à 700 MPa et qui peut être pliée à 180° sans défaut sous un diamètre intérieur de pliage inférieur à deux fois l'épaisseur de la tôle, utilisable notamment pour la mise en forme de pièces et présentant une transition fragile/ductile à une température inférieure à -50°C, tôle obtenue par le procédé selon les revendications 1 à 3, caractérisée en ce que la composition pondérale suivante :le reste, à l'exception des impuretés inhérentes à la fabrication, étant constitué par du fer, et comportant une microstructure de ferrite et bainite granulaire durcie par la précipitation des éléments de micro-alliage niobium-titane.carbone ≤ 0,1%,1 % ≤ manganèse ≤ 1,5 %silicium ≤ 0,3 %phosphore ≤ 0,03 %,soufre ≤ 0,01 %,0,01 % ≤ aluminium ≤ 0,1 %,0,04 % ≤ niobium ≤ 0,06 %,0,1 % ≤ titane ≤ 0,15%,0,1 %≤ molybdène ≤ 0,2 %,
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9507122 | 1995-06-15 | ||
| FR9507122A FR2735498B1 (fr) | 1995-06-15 | 1995-06-15 | Procede de realisation d'une bande de tole d'acier laminee a chaud a haute limite d'elasticite utlisable notamment pour la mise en forme |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0748877A1 EP0748877A1 (fr) | 1996-12-18 |
| EP0748877B1 true EP0748877B1 (fr) | 2001-03-07 |
Family
ID=9480017
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP96401263A Expired - Lifetime EP0748877B1 (fr) | 1995-06-15 | 1996-06-11 | Procédé de réalisation d'une bande de tôle d'acier laminée à chaud à très haute limite d'élasticité et tôle d'acier obtenue |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US5716464A (fr) |
| EP (1) | EP0748877B1 (fr) |
| AT (1) | ATE199575T1 (fr) |
| DE (1) | DE69611950T2 (fr) |
| ES (1) | ES2156985T3 (fr) |
| FR (1) | FR2735498B1 (fr) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP3417878B2 (ja) * | 1999-07-02 | 2003-06-16 | 株式会社神戸製鋼所 | 伸びフランジ性および疲労特性に優れた高強度熱延鋼板およびその製法 |
| WO2001023624A1 (fr) * | 1999-09-29 | 2001-04-05 | Nkk Corporation | Tole d'acier et son procede de fabrication |
| FR2801061B1 (fr) | 1999-11-12 | 2001-12-14 | Lorraine Laminage | Procede de realisation d'une bande de tole laminere a chaud a tres haute resistance, utilisable pour la mise en forme et notamment pour l'emboutissage |
| JP6252291B2 (ja) * | 2014-03-26 | 2017-12-27 | 新日鐵住金株式会社 | 鋼板及びその製造方法 |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| NL150851B (nl) * | 1971-04-20 | 1976-09-15 | Nippon Kokan Kk | Werkwijze ter bereiding van staal en daaruit gevormde voorwerpen. |
| US3976514A (en) * | 1975-02-10 | 1976-08-24 | Nippon Steel Corporation | Method for producing a high toughness and high tensil steel |
| DE2517164A1 (de) * | 1975-04-18 | 1976-10-21 | Rheinstahl Giesserei Ag | Verwendung einer schweissbaren, hoeherfesten stahllegierung fuer dickwandige stahlgusserzeugnisse |
| JPS6220821A (ja) * | 1985-07-17 | 1987-01-29 | Nippon Steel Corp | 高強度厚鋼板の製造法 |
| JP3031485B2 (ja) * | 1990-11-28 | 2000-04-10 | 川崎製鉄株式会社 | 降伏伸びに優れた高強度鉄筋の製造方法 |
| EP0535238A4 (en) * | 1991-03-13 | 1993-08-04 | Kawasaki Steel Corporation | High-strength steel sheet for forming and production thereof |
| WO1995026424A1 (fr) * | 1994-03-29 | 1995-10-05 | Nippon Steel Corporation | Tole grosse d'acier presentant d'excellentes caracteristiques sur le plan de la prevention de la propagation des criques et de la durete a basse temperature et procede d'elaboration de cette tole |
-
1995
- 1995-06-15 FR FR9507122A patent/FR2735498B1/fr not_active Expired - Fee Related
-
1996
- 1996-06-11 DE DE69611950T patent/DE69611950T2/de not_active Expired - Fee Related
- 1996-06-11 EP EP96401263A patent/EP0748877B1/fr not_active Expired - Lifetime
- 1996-06-11 ES ES96401263T patent/ES2156985T3/es not_active Expired - Lifetime
- 1996-06-11 AT AT96401263T patent/ATE199575T1/de not_active IP Right Cessation
- 1996-06-13 US US08/663,529 patent/US5716464A/en not_active Expired - Fee Related
Non-Patent Citations (1)
| Title |
|---|
| H. Berns, Stahlkunde für Ingenieure, 2. ed. juillet 1993, Springer Verlag, Berlin, p. 109-111 * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP0748877A1 (fr) | 1996-12-18 |
| ES2156985T3 (es) | 2001-08-01 |
| DE69611950D1 (de) | 2001-04-12 |
| FR2735498A1 (fr) | 1996-12-20 |
| ATE199575T1 (de) | 2001-03-15 |
| US5716464A (en) | 1998-02-10 |
| DE69611950T2 (de) | 2001-06-21 |
| FR2735498B1 (fr) | 1997-07-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2155915B2 (fr) | Procédé de fabrication de tôles d'acier laminées à froid et recuites à très haute résistance, et tôles ainsi produites | |
| CA2533023C (fr) | Procede de fabrication de toles d'acier austenitique fer-carbone-manganese, a haute resistance, excellente tenacite et aptitude a la mise en forme a froid, et toles ainsi produites | |
| CA2239478C (fr) | Acier inoxydable austenoferritique a tres bas nickel et presentant un fort allongement en traction | |
| EP1819461B1 (fr) | Procede de fabrication de toles d' acier austenitique , fer-carbone-manganese a tres hautes caracteristiques de resistance et excellente homogénéité. | |
| EP2718469B1 (fr) | Tôle d'acier laminée à froid et revêtue de zinc ou d'alliage de zinc, procede de fabrication et utilisation d'une telle tôle | |
| EP2155916B2 (fr) | Acier a faible densite presentant une bonne aptitude a l'emboutissage | |
| EP1913169B1 (fr) | Procede de fabrication de tôles d'acier presentant une haute resistance et une excellente ductilite, et tôles ainsi produites | |
| EP2630269B1 (fr) | Tole d'acier laminee a chaud ou a froid, son procede de fabrication et son utilisation dans l'industrie automobile | |
| EP3167091B1 (fr) | Tôle d'acier laminée à chaud et procédé de fabrication associé | |
| WO2007101921A1 (fr) | Procede de fabrication de tôles d1acier a tres hautes caracteristiques de resistance, de ductilite et de tenacite, et tôles ainsi produites | |
| EP1627092A1 (fr) | Tole laminee a froid et aluminiee en acier dual phase a tres haute resistance pour ceinture anti-implosion de televiseur, et procede de fabrication de cette tole | |
| CA2513096C (fr) | Acier lamine a chaud a tres haute resistance et procede de fabrication de bandes | |
| EP1099769B1 (fr) | Procédé de réalisation d'une bande de tôle laminée à chaud à très haute résistance, utilisable pour la mise en forme et notamment pour l'emboutissage | |
| CA2342256C (fr) | Acier lamine a chaud a tres haute limite d'elasticite et resistance mecanique utilisable notamment pour la realisation de piece de vehicules automobiles | |
| FR2833617A1 (fr) | Procede de fabrication de toles laminees a froid a tres haute resistance d'aciers dual phase micro-allies | |
| EP0748877A1 (fr) | Procédé de réalisation d'une bande de tÔle d'acier laminée à chaud à très haute limite d'élasticité et tÔle d'acier obtenue | |
| EP0481844B1 (fr) | Acier à soudabilité améliorée | |
| EP2103705A1 (fr) | Procédé de fabrication de tôles d'acier inoxydable austenitique à hautes caractèristiques mécaniques | |
| FR2795742A1 (fr) | Tole d'acier a moyen carbone calme a l'aluminium pour emballage | |
| FR2549490A1 (fr) | Procede pour la fabrication d'une piece forgee en acier faiblement allie | |
| FR2748033A1 (fr) | Procede de realisation d'une bande de tole d'acier laminee a chaud a tres haute resistance utilisable pour la mise en forme et notamment pour l'emboutissage |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU NL PT SE |
|
| 17P | Request for examination filed |
Effective date: 19961227 |
|
| 17Q | First examination report despatched |
Effective date: 19990427 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI LU NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20010307 |
|
| REF | Corresponds to: |
Ref document number: 199575 Country of ref document: AT Date of ref document: 20010315 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 20010307 |
|
| REF | Corresponds to: |
Ref document number: 69611950 Country of ref document: DE Date of ref document: 20010412 |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: SOLLAC |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: FRENCH |
|
| ITF | It: translation for a ep patent filed | ||
| NLT2 | Nl: modifications (of names), taken from the european patent patent bulletin |
Owner name: SOLLAC |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20010607 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20010607 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20010608 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2156985 Country of ref document: ES Kind code of ref document: T3 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 20030515 Year of fee payment: 8 Ref country code: AT Payment date: 20030515 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 20030519 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20030520 Year of fee payment: 8 Ref country code: NL Payment date: 20030520 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20030603 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FI Payment date: 20030604 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20030611 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20030612 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20030616 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20030709 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040611 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040611 Ref country code: FI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040611 Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040611 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040612 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040612 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040630 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040630 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20040630 |
|
| BERE | Be: lapsed |
Owner name: S.A. *SOLLAC Effective date: 20040630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050101 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050101 |
|
| EUG | Se: european patent has lapsed | ||
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20040611 |
|
| EUG | Se: european patent has lapsed | ||
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20050228 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 20050101 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050611 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20040612 |