EP0576348B1 - TÔle revêtue et procédé de fabrication de cette tÔle - Google Patents
TÔle revêtue et procédé de fabrication de cette tÔle Download PDFInfo
- Publication number
- EP0576348B1 EP0576348B1 EP93401601A EP93401601A EP0576348B1 EP 0576348 B1 EP0576348 B1 EP 0576348B1 EP 93401601 A EP93401601 A EP 93401601A EP 93401601 A EP93401601 A EP 93401601A EP 0576348 B1 EP0576348 B1 EP 0576348B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- film
- sheet
- aluminium
- deposited
- sheet metal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 12
- 238000000034 method Methods 0.000 title claims description 14
- 229910052751 metal Inorganic materials 0.000 claims abstract description 35
- 239000002184 metal Substances 0.000 claims abstract description 35
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 claims abstract description 27
- 229910052782 aluminium Inorganic materials 0.000 claims abstract description 22
- 238000005260 corrosion Methods 0.000 claims abstract description 14
- 230000007797 corrosion Effects 0.000 claims abstract description 14
- 239000000395 magnesium oxide Substances 0.000 claims abstract description 14
- CPLXHLVBOLITMK-UHFFFAOYSA-N magnesium oxide Inorganic materials [Mg]=O CPLXHLVBOLITMK-UHFFFAOYSA-N 0.000 claims abstract description 14
- AXZKOIWUVFPNLO-UHFFFAOYSA-N magnesium;oxygen(2-) Chemical compound [O-2].[Mg+2] AXZKOIWUVFPNLO-UHFFFAOYSA-N 0.000 claims abstract description 14
- 239000000758 substrate Substances 0.000 claims abstract description 14
- VYZAMTAEIAYCRO-UHFFFAOYSA-N Chromium Chemical compound [Cr] VYZAMTAEIAYCRO-UHFFFAOYSA-N 0.000 claims abstract description 10
- 239000004411 aluminium Substances 0.000 claims abstract description 10
- 239000011651 chromium Substances 0.000 claims abstract description 9
- 229910052804 chromium Inorganic materials 0.000 claims abstract description 9
- 229910000838 Al alloy Inorganic materials 0.000 claims abstract description 8
- FYYHWMGAXLPEAU-UHFFFAOYSA-N Magnesium Chemical compound [Mg] FYYHWMGAXLPEAU-UHFFFAOYSA-N 0.000 claims abstract description 8
- 229910052749 magnesium Inorganic materials 0.000 claims abstract description 7
- 239000011777 magnesium Substances 0.000 claims abstract description 7
- 239000011248 coating agent Substances 0.000 claims description 17
- 238000000576 coating method Methods 0.000 claims description 17
- 229910000831 Steel Inorganic materials 0.000 claims description 13
- 239000010959 steel Substances 0.000 claims description 13
- 150000002500 ions Chemical class 0.000 claims description 12
- 239000000463 material Substances 0.000 claims description 11
- 229910045601 alloy Inorganic materials 0.000 claims description 9
- 239000000956 alloy Substances 0.000 claims description 9
- 238000005507 spraying Methods 0.000 claims description 7
- 229910000861 Mg alloy Inorganic materials 0.000 claims description 4
- 229910000676 Si alloy Inorganic materials 0.000 claims description 4
- 150000001875 compounds Chemical class 0.000 claims description 4
- QDOXWKRWXJOMAK-UHFFFAOYSA-N dichromium trioxide Chemical compound O=[Cr]O[Cr]=O QDOXWKRWXJOMAK-UHFFFAOYSA-N 0.000 claims description 4
- 229910000599 Cr alloy Inorganic materials 0.000 claims description 3
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 claims description 3
- 239000000788 chromium alloy Substances 0.000 claims description 3
- 239000011701 zinc Substances 0.000 claims description 3
- 229910052725 zinc Inorganic materials 0.000 claims description 3
- 239000010935 stainless steel Substances 0.000 claims description 2
- 229910001220 stainless steel Inorganic materials 0.000 claims description 2
- 238000001771 vacuum deposition Methods 0.000 claims description 2
- 238000010791 quenching Methods 0.000 claims 1
- 230000000171 quenching effect Effects 0.000 claims 1
- 238000010884 ion-beam technique Methods 0.000 abstract description 6
- 238000003618 dip coating Methods 0.000 abstract description 3
- WGLPBDUCMAPZCE-UHFFFAOYSA-N Trioxochromium Chemical compound O=[Cr](=O)=O WGLPBDUCMAPZCE-UHFFFAOYSA-N 0.000 abstract description 2
- 229910000423 chromium oxide Inorganic materials 0.000 abstract description 2
- 229910001092 metal group alloy Inorganic materials 0.000 abstract description 2
- 238000012360 testing method Methods 0.000 description 17
- 229910000680 Aluminized steel Inorganic materials 0.000 description 12
- JEIPFZHSYJVQDO-UHFFFAOYSA-N iron(III) oxide Inorganic materials O=[Fe]O[Fe]=O JEIPFZHSYJVQDO-UHFFFAOYSA-N 0.000 description 10
- 238000000151 deposition Methods 0.000 description 6
- 230000001681 protective effect Effects 0.000 description 5
- 239000000243 solution Substances 0.000 description 5
- 230000008021 deposition Effects 0.000 description 4
- 238000007598 dipping method Methods 0.000 description 4
- 238000007654 immersion Methods 0.000 description 4
- 230000004580 weight loss Effects 0.000 description 4
- FAPWRFPIFSIZLT-UHFFFAOYSA-M Sodium chloride Chemical compound [Na+].[Cl-] FAPWRFPIFSIZLT-UHFFFAOYSA-M 0.000 description 3
- SNAAJJQQZSMGQD-UHFFFAOYSA-N aluminum magnesium Chemical compound [Mg].[Al] SNAAJJQQZSMGQD-UHFFFAOYSA-N 0.000 description 3
- 238000005452 bending Methods 0.000 description 3
- 239000007789 gas Substances 0.000 description 3
- 239000000203 mixture Substances 0.000 description 3
- 238000007493 shaping process Methods 0.000 description 3
- CSCPPACGZOOCGX-UHFFFAOYSA-N Acetone Chemical compound CC(C)=O CSCPPACGZOOCGX-UHFFFAOYSA-N 0.000 description 2
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 description 2
- QAOWNCQODCNURD-UHFFFAOYSA-N Sulfuric acid Chemical compound OS(O)(=O)=O QAOWNCQODCNURD-UHFFFAOYSA-N 0.000 description 2
- QQHSIRTYSFLSRM-UHFFFAOYSA-N alumanylidynechromium Chemical compound [Al].[Cr] QQHSIRTYSFLSRM-UHFFFAOYSA-N 0.000 description 2
- 238000005269 aluminizing Methods 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 2
- 238000006243 chemical reaction Methods 0.000 description 2
- 238000004532 chromating Methods 0.000 description 2
- 238000005336 cracking Methods 0.000 description 2
- 239000013078 crystal Substances 0.000 description 2
- PYRZPBDTPRQYKG-UHFFFAOYSA-N cyclopentene-1-carboxylic acid Chemical compound OC(=O)C1=CCCC1 PYRZPBDTPRQYKG-UHFFFAOYSA-N 0.000 description 2
- 239000003921 oil Substances 0.000 description 2
- 239000011780 sodium chloride Substances 0.000 description 2
- 239000000126 substance Substances 0.000 description 2
- 241001163841 Albugo ipomoeae-panduratae Species 0.000 description 1
- PNEYBMLMFCGWSK-UHFFFAOYSA-N Alumina Chemical class [O-2].[O-2].[O-2].[Al+3].[Al+3] PNEYBMLMFCGWSK-UHFFFAOYSA-N 0.000 description 1
- VHUUQVKOLVNVRT-UHFFFAOYSA-N Ammonium hydroxide Chemical compound [NH4+].[OH-] VHUUQVKOLVNVRT-UHFFFAOYSA-N 0.000 description 1
- 241001631457 Cannula Species 0.000 description 1
- LFQSCWFLJHTTHZ-UHFFFAOYSA-N Ethanol Chemical compound CCO LFQSCWFLJHTTHZ-UHFFFAOYSA-N 0.000 description 1
- VEXZGXHMUGYJMC-UHFFFAOYSA-N Hydrochloric acid Chemical compound Cl VEXZGXHMUGYJMC-UHFFFAOYSA-N 0.000 description 1
- GRYLNZFGIOXLOG-UHFFFAOYSA-N Nitric acid Chemical compound O[N+]([O-])=O GRYLNZFGIOXLOG-UHFFFAOYSA-N 0.000 description 1
- XUIMIQQOPSSXEZ-UHFFFAOYSA-N Silicon Chemical compound [Si] XUIMIQQOPSSXEZ-UHFFFAOYSA-N 0.000 description 1
- 230000002378 acidificating effect Effects 0.000 description 1
- CSDREXVUYHZDNP-UHFFFAOYSA-N alumanylidynesilicon Chemical compound [Al].[Si] CSDREXVUYHZDNP-UHFFFAOYSA-N 0.000 description 1
- 239000000908 ammonium hydroxide Substances 0.000 description 1
- 239000007864 aqueous solution Substances 0.000 description 1
- 229910052786 argon Inorganic materials 0.000 description 1
- 230000003197 catalytic effect Effects 0.000 description 1
- 239000003153 chemical reaction reagent Substances 0.000 description 1
- 230000007423 decrease Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 230000008020 evaporation Effects 0.000 description 1
- 238000001704 evaporation Methods 0.000 description 1
- IXCSERBJSXMMFS-UHFFFAOYSA-N hcl hcl Chemical compound Cl.Cl IXCSERBJSXMMFS-UHFFFAOYSA-N 0.000 description 1
- 239000013072 incoming material Substances 0.000 description 1
- 238000010849 ion bombardment Methods 0.000 description 1
- UQSXHKLRYXJYBZ-UHFFFAOYSA-N iron oxide Inorganic materials [Fe]=O UQSXHKLRYXJYBZ-UHFFFAOYSA-N 0.000 description 1
- 235000013980 iron oxide Nutrition 0.000 description 1
- VBMVTYDPPZVILR-UHFFFAOYSA-N iron(2+);oxygen(2-) Chemical class [O-2].[Fe+2] VBMVTYDPPZVILR-UHFFFAOYSA-N 0.000 description 1
- 238000005461 lubrication Methods 0.000 description 1
- 239000007769 metal material Substances 0.000 description 1
- 239000003595 mist Substances 0.000 description 1
- 229910017604 nitric acid Inorganic materials 0.000 description 1
- 238000002161 passivation Methods 0.000 description 1
- 150000003839 salts Chemical class 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/02—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings only including layers of metallic material
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
-
- C—CHEMISTRY; METALLURGY
- C23—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; CHEMICAL SURFACE TREATMENT; DIFFUSION TREATMENT OF METALLIC MATERIAL; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL; INHIBITING CORROSION OF METALLIC MATERIAL OR INCRUSTATION IN GENERAL
- C23C—COATING METALLIC MATERIAL; COATING MATERIAL WITH METALLIC MATERIAL; SURFACE TREATMENT OF METALLIC MATERIAL BY DIFFUSION INTO THE SURFACE, BY CHEMICAL CONVERSION OR SUBSTITUTION; COATING BY VACUUM EVAPORATION, BY SPUTTERING, BY ION IMPLANTATION OR BY CHEMICAL VAPOUR DEPOSITION, IN GENERAL
- C23C28/00—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D
- C23C28/02—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings only including layers of metallic material
- C23C28/023—Coating for obtaining at least two superposed coatings either by methods not provided for in a single one of groups C23C2/00 - C23C26/00 or by combinations of methods provided for in subclasses C23C and C25C or C25D only coatings only including layers of metallic material only coatings of metal elements only
Definitions
- the present invention relates to a coated sheet and a process for the manufacture of this sheet.
- Aluminized steel sheets are manufactured usually "hot-soaked” that is to say immersing the sheet in a bath of molten aluminum-silicon alloy. These dip coatings have a thickness greater than 7 ⁇ m, and preferably greater than 10 ⁇ m.
- this type of dip coating it is created, at the interface between the sheet and the coating, a transition zone made of an intermediate alloy. During subsequent shaping operations, this intermediate alloy can easily crack. This risk of cracking reduces the resistance of the sheets to corrosion.
- the metal layer solidified on the surface generally has a polymorphic crystal structure. Therefore, when the sheets are subjected to aggressive atmospheres, electrochemical effects appear between crystals of different structures of the layer, which cause local decreases thickness of the protective metal layer. In order to maintain good corrosion protection it it is therefore necessary that the coating is sufficiently thick; but, conversely, during subsequent operations of shaping, this coating risks all the more to crack that it's thick.
- Aluminized steel sheets are used by example for the manufacture of different elements of a vehicle exhaust line, or for manufacturing oven walls; these sheets have a greater thickness 0.3 mm, and preferably greater than 0.5 mm.
- the aluminized steel sheets resist more for a long time with aggressive atmospheres than steel sheets ordinary.
- the aggressive atmospheres to which are subjected the aluminized sheets cause at the end the appearance of rust on their surface for some time.
- rust appears "white” corresponding to the formation of aluminum oxides whitish.
- rust appears "red” corresponding to the formation of iron oxides.
- Chromatization is generally applied by immersion of the aluminized sheet in a treatment bath.
- This bath is consisting of an acidic aqueous solution containing chromium in the form of ions.
- the aluminized sheet reacts with the solution and a conversion layer is formed protective.
- Chromating of aluminized steel sheets helps delay the onset of white rust. However, red rust appears as soon as the coating of the sheet is cracked or punctured.
- JP-A-117 877, JP-A-1 132 778 and FR-A-2 550 555 each describe a coated sheet of the type comprising a steel substrate, a metal layer containing mainly aluminum or zinc deposited on at least one of the faces of the substrate, and at least one film covering the metallic layer.
- the object of the invention is in particular to improve the corrosion resistance of coated steel sheets, especially particularly aluminized steel sheets, this by optimizing the ability to deform the sheet in order to avoid cracking of its coating by folding.
- the subject of the invention is a coated sheet of the aforementioned type, characterized in that the metal layer is deposited by dipping and has a thickness greater than 7 ⁇ m, in that the film comprises a material chosen from aluminum alloys -chrome (Al-Cr), aluminum-magnesium alloys (Al-Mg), magnesium oxide (MgO) and chromium oxide (Cr 2 O 3 ), and in that the film thickness is at most equal to 1 mm.
- Al-Cr aluminum alloys -chrome
- Al-Mg aluminum-magnesium alloys
- MgO magnesium oxide
- Cr 2 O 3 chromium oxide
- the invention also relates to a method for the manufacture of a coated sheet as defined above, characterized in that the coating film is deposited by vacuum deposition.
- the invention also relates to the use of a sheet as defined above for the manufacture elements of a vehicle exhaust line.
- the invention also relates to the application of process as defined above for the protection of a sheet made of steel against corrosion.
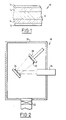
- This sheet 10 comprises a sheet 12 of steel, in particular steel stainless, forming a substrate, covered on both sides a metal layer 14 mainly comprising aluminum.
- the layer 14 has a thickness of between 10 and 30 ⁇ m.
- This layer 14 is covered with a film 16 of a thickness at most equal to 1 ⁇ m, preferably at most equal to 0.20 ⁇ m, comprising a metal alloy such as an aluminum alloy containing chromium or magnesium or an oxide such as magnesium oxide (MgO) or chromium oxide (Cr 2 O 3 ).
- the material constituting the film 16 is chosen from aluminum-chromium alloys (Al-Cr), aluminum-magnesium alloys (Al-Mg) and magnesium oxide.
- the sheet 10 is intended in particular for the manufacture of vehicle exhaust line components, for example cannulas, silencers, resonators, catalytic converters and elements tubular such as primary downspouts.
- vehicle exhaust line components for example cannulas, silencers, resonators, catalytic converters and elements tubular such as primary downspouts.
- the film 16 consists of an alloy comprising, by mass, approximately 22% of aluminum and approximately 78% of chromium, in the form of an AlCr 2 compound.
- the film 16 has a thickness of approximately 0.1 ⁇ m.
- the film 16 consists of an alloy comprising, by mass, approximately 88% of aluminum and approximately 12% of magnesium. In this case, the film 16 has a thickness of 0.20 ⁇ m.
- the film 16 is made of magnesium oxide.
- the film 16 has a thickness of 0.20 ⁇ m.
- the sheet After aluminizing, the sheet is cleaned according to a known process, for example using acetone and alcohol.
- a film 16 is then deposited on the layers 14 of each of the faces of the sheet 12.
- the film is deposited by ion spraying under vacuum of incoming materials in the composition of the film.
- FIG. 2 shows an example of device 18, of known type, making it possible to carry out the deposition of a film 16 by ion spraying under vacuum.
- the device 18 comprises an enclosure 20 in which maintains a high vacuum by means of several vacuum pumps 22 of which only one is shown at Figure 2.
- the surface of a target 24, comprising the materials used in the composition of the film 16, is sprayed by means of a high intensity ion beam from a source 26.
- the sheet 10 to be coated with a film is carried by a support 28 disposed opposite the target 24.
- the ion source 26 is for example of the type KAUFMAN.
- the source 26 is supplied by a gas which is ionized to form an ion beam.
- the gas used is argon.
- the energy of the Ar + ions is approximately 1.2 keV.
- the current density of the ion beam is approximately 1.6 mA / cm 2 .
- the pressure in the enclosure 20 is approximately 10 -2 Pa during the evaporation of the surface of the target 24.
- the ion spraying can be carried out under other conditions than those of the example.
- the Ar + ions can have an energy between 0.5 and 2 keV
- the Ar + ion beam can have a current density between 0.5 and 4 mA / cm 2 .
- the components of target 24 are sprayed by the ion beam and deposit on the sheet 10 arranged next to the target.
- the target 24 comprises, by mass, approximately 22% of aluminum and approximately 78% of chromium.
- the ion bombardment of this target makes it possible to deposit on the sheet 10 a film 16 comprising, the same proportions of aluminum and chromium, the alloy being in the form of an AlCr 2 compound.
- target 24 includes aluminum and magnesium in suitable proportions to deposit on the sheet 10 a film 16 comprising, by mass, approximately 88% of aluminum and about 12% magnesium.
- target 24 contains magnesium oxide of so as to deposit on the sheet 10 a film 16 of the same material.
- Salt spray tests have been performed by subjecting the sheets to a mist containing 5% of sodium chloride.
- Red rust appears on the surface of the Alusi sheet 576 hours after the start of testing.
- the sheet metal surface is covered with red rust at most 50% 672 hours after the start of the tests.
- Red rust appears on the surface of the sheet metal coated with Al-Mg film 912 hours after the start tests. Red rust covers more than 50% of the sheet surface 1000 hours after the start of the tests.
- Red rust appears on the surface of the sheet coated with MgO 1344 film hours after the start of tests.
- the film 16 deposited on the aluminized steel sheet allows you to double the time before the onset of red rust on the sheet compared to a steel sheet aluminized without film 16.
- the sheets undergoing the resistance tests to condensates are covered on one side only with a coating comprising, depending on the sheets, a layer 14 metallic mainly comprising aluminum without film 16 (Alusi sheet), or a metal layer 14 mainly containing aluminum with a film 16. Only the coated side is exposed to condensate.
- the weight loss of Alusi sheet is 300g / m 2 .
- the weight loss of the sheet coated with an MgO film is 160 g / m 2 .
- the weight loss of a sheet coated with an Al-Mg film is 140 g / m 2 .
- the weight loss of the sheet coated with an Al-Cr film is 135 g / m 2 .
- the sheet is folded at 180 ° C by inserting into the fold a certain number of shims of the same thickness E as the sheet tested. We observe from how many holds the sheet metal coating is not cracked depending on its thickness.
- the coating of the Alusi sheet does not contain crack when four shims are inserted in the fold, and many cracks when three wedges are inserted in the fold.
- the coating of the sheet comprising an Al-Mg film has an identical behavior to that of Alusi sheet.
- the coating of the sheet with an Al-Cr film has one to two cracks when three shims are interspersed in the fold.
- the invention is not limited to the examples of realization described.
- the sheet 12 forming a substrate can be formed by other materials than steel.
- Layer 14 containing mainly aluminum can be replaced by a layer containing a other metallic material especially by a layer containing mainly zinc deposited by dipping.
- the layer 14 and the film 16 can be arranged on one side of the sheet 12 forming a substrate.
- Al-Cr aluminum chromium alloys
- Al-Mg aluminum-magnesium alloys
- MgO magnesium oxide
- Cr 2 O 3 chromium oxide
- the film can be vacuum deposited by other physical means than that described.
- the deposit under film vacuum can also be done by route chemical using reagents in the form of gas.
- the invention has many advantages.
- the protective film is very thin and can be quickly deposited on a sheet.
- the film deposition speed is compatible with the speeds usual manufacturing of aluminized sheets.
- the protective film does not present no danger to the environment.
- the deposition of the metal layer carried out at hardened optimizes the roughness characteristics coating and therefore facilitate the sheet lubrication during the subsequent stages of sheet metal shaping.
Landscapes
- Chemical & Material Sciences (AREA)
- Chemical Kinetics & Catalysis (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physical Vapour Deposition (AREA)
- Other Surface Treatments For Metallic Materials (AREA)
- Laminated Bodies (AREA)
- Application Of Or Painting With Fluid Materials (AREA)
- Paper (AREA)
Description
- le film comporte un alliage comprenant, en masse, 88% environ d'aluminium et 12% environ de magnésium ;
- le film comporte un alliage comprenant, en masse, 22% environ d'aluminium et 78% environ de chrome, sous forme de composé AlCr2 ;
- le substrat métallique est en acier inoxydable;
- le film a une épaisseur au plus égale à 0,20 mm.
- la couche métallique est déposée sur le substrat par immersion de ce substrat dans un bain d'alliage fondu d'aluminium et de silicium ;
- le dépôt du film est effectué par pulvérisation ionique d'au moins une cible contenant les matériaux destinés à composer le film ;
- la surface de la cible est pulvérisée par un faisceau d'ions Ar+ ayant une énergie comprise entre 0,5 et 2 keV, de préférence égale à 1,2 keV, le faisceau ayant une densité de courant comprise entre 0,5 et 4 mA/cm2, de préférence égale à 1,6 mA/cm2, la pression dans l'enceinte sous vide étant d'environ 10-2 Pa pendant la pulvérisation de la surface de la cible.
- la figure 1 est une vue en coupe d'une tôle revêtue selon l'invention ;
- la figure 2 est une vue schématique en élévation en coupe d'un dispositif pour le dépôt d'un film sur une tôle en acier aluminié.
Claims (11)
- Tôle revêtue du type comprenant un substrat (12) en acier, une couche (14) métallique contenant principalement de l'aluminium ou du zinc déposée sur au moins une des faces du substrat, et au moins un film (16) recouvrant la couche métallique, caractérisée en ce que la couche métallique (14) est déposée au trempé et a une épaisseur supérieure à 7 µm, en ce que le film (16) comprend un matériau choisi parmi les alliages aluminium-chrome (Al-Cr), les alliages aluminium-magnésium (Al-Mg), l'oxyde de magnésium (MgO) et l'oxyde de chrome (Cr2O3), et en ce que l'épaisseur du film est au plus égale à 1 µm.
- Tôle selon la revendication 1, caractérisée en ce que le film (16) comporte un alliage comprenant, en masse, 88% environ d'aluminium et 12% environ de magnésium.
- Tôle selon la revendication 1, caractérisée en ce que le film (16) comporte un alliage comprenant, en masse, 22% environ d'aluminium et 78% environ de chrome, sous forme de composé AlCr2.
- Tôle selon l'une quelconque des revendications précédentes, caractérisée en ce que le substrat métallique (12) est en acier inoxydable.
- Tôle selon l'une quelconque des revendications précédentes, caractérisée en ce que le film (16) a une épaisseur au plus égale à 0,20 µm.
- Procédé pour la fabrication d'une tôle revêtue selon l'une quelconque des revendications précédentes, caractérisé en ce que le film de revêtement est déposé par dépôt sous vide.
- Procédé selon la revendication 6, caractérisé en ce que la couche métallique (14) est déposée sur le substrat (12) par immersion de ce substrat (12) dans un bain d'alliage fondu d'aluminium et de silicium.
- Procédé selon la revendication 6 ou 7, caractérisé par le fait que le dépôt du film (16) est effectué par pulvérisation ionique d'au moins une cible (24) contenant les matériaux destinés à composer le film (16).
- Procédé selon la revendication 8, caractérisé par le fait que la surface de la cible (24) est pulvérisée par un faisceau d'ions Ar+ ayant une énergie comprise entre 0,5 et 2 keV, de préférence égale à 1,2 keV, le faisceau ayant une densité de courant comprise entre 0,5 et 4 mA/cm2, de préférence égale à 1,6 mA/cm2, la pression dans l'enceinte (20) sous vide étant d'environ 10-2 Pa pendant la pulvérisation de la surface de la cible (24).
- Utilisation d'une tôle selon l'une quelconque des revendications 1 à 5 pour la fabrication d'éléments d'une ligne d'échappement de véhicule.
- Application du procédé selon l'une quelconque des revendications 6 à 9, à la protection d'une tôle en acier contre la corrosion.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9207585A FR2692596B1 (fr) | 1992-06-22 | 1992-06-22 | Tôle revêtue et procédé de fabrication de cette tôle. |
| FR9207585 | 1992-06-22 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0576348A1 EP0576348A1 (fr) | 1993-12-29 |
| EP0576348B1 true EP0576348B1 (fr) | 1998-04-29 |
Family
ID=9431012
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP93401601A Expired - Lifetime EP0576348B1 (fr) | 1992-06-22 | 1993-06-22 | TÔle revêtue et procédé de fabrication de cette tÔle |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP0576348B1 (fr) |
| AT (1) | ATE165630T1 (fr) |
| DE (1) | DE69318217T2 (fr) |
| ES (1) | ES2115739T3 (fr) |
| FR (1) | FR2692596B1 (fr) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE19527515C1 (de) * | 1995-07-27 | 1996-11-28 | Fraunhofer Ges Forschung | Verfahren zur Herstellung von korrosionsgeschütztem Stahlblech |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE2103984A1 (en) * | 1971-01-28 | 1972-09-14 | Metallisator Korrosionsschutzt | Protecting car exhaust pipes - against corrosion by coating with aluminium layer further coated by zinc |
| FR2550555B2 (fr) * | 1983-03-03 | 1988-12-30 | Zincroksid Spa | Procede pour la protection de lamines plats en acier zingue au moyen d'un revetement electrolytique multicouche |
| DE3512176A1 (de) * | 1985-04-03 | 1986-10-09 | Winfried 7758 Meersburg Heinzel | Verfahren zur oberflaechenbehandlung eines druckmaschinenzylinders |
| EP0410627A1 (fr) * | 1989-07-27 | 1991-01-30 | Kabushiki Kaisha Toshiba | Couche d'oxyde avec orientation de cristal préferée, procédé de sa production et matériau d'enregistrement magnéto-optique |
| FR2664617B1 (fr) * | 1990-07-16 | 1993-08-06 | Lorraine Laminage | Procede de revetement d'aluminium par trempe a chaud d'une bande d'acier et bande d'acier obtenue par ce procede. |
| JPH1017877A (ja) * | 1996-06-28 | 1998-01-20 | Ube Ind Ltd | 廃棄物の処理方法および装置 |
| JPH1132778A (ja) * | 1997-07-24 | 1999-02-09 | Suntory Ltd | 新規セリンプロテアーゼ |
-
1992
- 1992-06-22 FR FR9207585A patent/FR2692596B1/fr not_active Expired - Fee Related
-
1993
- 1993-06-22 DE DE69318217T patent/DE69318217T2/de not_active Expired - Lifetime
- 1993-06-22 AT AT93401601T patent/ATE165630T1/de active
- 1993-06-22 EP EP93401601A patent/EP0576348B1/fr not_active Expired - Lifetime
- 1993-06-22 ES ES93401601T patent/ES2115739T3/es not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| DE69318217D1 (de) | 1998-06-04 |
| FR2692596B1 (fr) | 1995-03-31 |
| EP0576348A1 (fr) | 1993-12-29 |
| ES2115739T3 (es) | 1998-07-01 |
| ATE165630T1 (de) | 1998-05-15 |
| FR2692596A1 (fr) | 1993-12-24 |
| DE69318217T2 (de) | 1998-10-01 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN113316664B (zh) | 合金涂覆钢板及其制造方法 | |
| US4963440A (en) | Al-Cr alloy vapor-deposited material | |
| JP2008513595A (ja) | 金属被覆鋼製品の製造のための方法と装置 | |
| US10001588B2 (en) | Enhanced, protected silver coatings on aluminum for optical mirror and method of making same | |
| EP0884403A1 (fr) | Materiau multicouches à revetement anti-erosion, anti-abrasion, et anti-usure sur substrat en aluminium, en magnesium ou en leurs alliages. | |
| WO2012080581A1 (fr) | Tôle d'acier comprenant un revêtement multicouche | |
| US7645494B2 (en) | Pre-plating surface treatments for enhanced galvanic-corrosion resistance | |
| EP0132424B1 (fr) | Fil d'acier à revêtements superposés résistant à la corrosion | |
| KR101353451B1 (ko) | 도금강판 및 이의 제조방법 | |
| EP0576348A1 (fr) | Tôle revêtue et procédé de fabrication de cette tôle | |
| JP3545051B2 (ja) | 耐食性に優れたZn−Mg系めっき鋼板及び製造方法 | |
| JPH0881761A (ja) | Zn−Mg合金めっき鋼板及び製造方法 | |
| KR0166099B1 (ko) | 내식성이 우수한 알루미늄-규소-크롬계 도금강판 및 그 제조방법 | |
| JP2912029B2 (ja) | 合金化亜鉛めっき鋼板 | |
| EP1600525B1 (fr) | Procédé de fabrication ou de réparation d'un revêtement sur un substrat métallique | |
| KR100421948B1 (ko) | 복합코팅된 티타늄 알루미나이드계 합금 | |
| EP0453432B1 (fr) | Procédé pour former un revêtement de zinc-aluminium sur une bande d'acier | |
| JPH05320946A (ja) | 溶融亜鉛めっき鋼板及び合金化溶融亜鉛めっき鋼板の製造方法 | |
| JP2000096206A (ja) | 耐高温溶射被覆部材 | |
| JP2002226959A (ja) | 加工性に優れた溶融Al系めっき鋼板およびその製造方法 | |
| JPH02290961A (ja) | 加工性に優れた蒸着a1めっき鋼板の製造方法 | |
| FR2656632A1 (fr) | Procede de revetement de surfaces comprenant un depot metallurgique prealable d'au moins une couche d'aluminium et son anodisation dure, pieces traitees suivant ce procede, et procede de collage desdites pieces. | |
| JPH1018052A (ja) | 硬質めっき皮膜被覆部材とその製造方法 | |
| KR20130074648A (ko) | 도금 강판 및 이의 제조방법 | |
| FR2575767A1 (fr) | Procede de depot d'un revetement protecteur sur des pieces metalliques a base de titane ou d'un alliage de titane |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FR GB GR IT LI LU NL PT SE |
|
| 17P | Request for examination filed |
Effective date: 19940504 |
|
| 17Q | First examination report despatched |
Effective date: 19970128 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FR GB GR IT LI LU NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980429 |
|
| REF | Corresponds to: |
Ref document number: 165630 Country of ref document: AT Date of ref document: 19980515 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| ITF | It: translation for a ep patent filed | ||
| REF | Corresponds to: |
Ref document number: 69318217 Country of ref document: DE Date of ref document: 19980604 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980630 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980630 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2115739 Country of ref document: ES Kind code of ref document: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980729 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19980729 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19980730 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20120524 Year of fee payment: 20 Ref country code: NL Payment date: 20120530 Year of fee payment: 20 Ref country code: LU Payment date: 20120525 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 20120524 Year of fee payment: 20 Ref country code: SE Payment date: 20120525 Year of fee payment: 20 Ref country code: FR Payment date: 20120705 Year of fee payment: 20 Ref country code: GB Payment date: 20120525 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20120526 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20120614 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20120524 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 69318217 Country of ref document: DE |
|
| BE20 | Be: patent expired |
Owner name: *SOLLAC Effective date: 20130622 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V4 Effective date: 20130622 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20130621 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20130621 Ref country code: DE Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20130625 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 165630 Country of ref document: AT Kind code of ref document: T Effective date: 20130622 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20140828 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20130623 |