EP0339297B1 - Vorrichtung zum Aufnehmen von Gegenständen und zum Zuführen derselben zu längs eines Transportweges angeordneten, aufeinanderfolgenden Be- oder Verarbeitungsstationen - Google Patents
Vorrichtung zum Aufnehmen von Gegenständen und zum Zuführen derselben zu längs eines Transportweges angeordneten, aufeinanderfolgenden Be- oder Verarbeitungsstationen Download PDFInfo
- Publication number
- EP0339297B1 EP0339297B1 EP89105774A EP89105774A EP0339297B1 EP 0339297 B1 EP0339297 B1 EP 0339297B1 EP 89105774 A EP89105774 A EP 89105774A EP 89105774 A EP89105774 A EP 89105774A EP 0339297 B1 EP0339297 B1 EP 0339297B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- objects
- sequence
- transportation
- stations
- containers
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 230000008878 coupling Effects 0.000 claims description 5
- 238000010168 coupling process Methods 0.000 claims description 5
- 238000005859 coupling reaction Methods 0.000 claims description 5
- 238000002372 labelling Methods 0.000 claims description 4
- 238000003754 machining Methods 0.000 claims description 3
- 230000006978 adaptation Effects 0.000 claims 1
- 238000007789 sealing Methods 0.000 description 3
- 238000005352 clarification Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/005—Adjustable conveying means
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B43/00—Forming, feeding, opening or setting-up containers or receptacles in association with packaging
- B65B43/42—Feeding or positioning bags, boxes, or cartons in the distended, opened, or set-up state; Feeding preformed rigid containers, e.g. tins, capsules, glass tubes, glasses, to the packaging position; Locating containers or receptacles at the filling position; Supporting containers or receptacles during the filling operation
- B65B43/54—Means for supporting containers or receptacles during the filling operation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B59/00—Arrangements to enable machines to handle articles of different sizes, to produce packages of different sizes, to vary the contents of packages, to handle different types of packaging material, or to give access for cleaning or maintenance purposes
- B65B59/003—Arrangements to enable adjustments related to the packaging material
Definitions
- the invention relates to a device for picking up objects and for feeding them to successive processing or processing stations arranged along a transport path, in particular as a filling system for picking up containers from a denesting station and for feeding them to filling, lid placement, sealing, labeling - And removal stations or the like, with a base frame, a transport device mounted thereon with receptacles for the objects, which are arranged one after the other in the transport direction and the shape of which is adapted to the objects, and a clock drive, for a gradual advance of the transport device by the same stride lengths worries.
- the transport device has receptacles for only one and the same shape and size of containers, for example as a chain or endless chains parallel to one another, which run parallel to one another and have plates with cup receptacles fastened in the transverse direction between each of them on a chain link , wherein the cup receptacles are holes whose diameter is adapted to the diameter of the cups to be filled in each case, which have upper edges with which they are supported on the edges of the holes.
- These cups have to are not necessarily round, but can also have a rectangular shape, for example. It is understood that the receptacles in the receiving plates are each adapted to the shape of the container used.
- all the receiving plates are intended for the same cup size and cup shape, so that only this special cup shape and size can be unstacked, filled, sealed, and if necessary labeled and removed.
- the existing mounting plates had to be replaced by hand with other mounting plates that had recordings that were adapted to the changed container shape and size .
- the device could then start up again and gradually transport the containers to be filled from station to station in accordance with the clock drive.
- the object on which the invention is based is seen in creating a device of the type described, in which a changeover to a different cup shape or cup size can be carried out without considerable expenditure on changeover time and changeover work.
- This object is achieved according to the invention in that, in order to adapt to a predetermined sequence of at least two differently shaped objects which are to be machinable and / or processable by means of the device, the transport device in the transport direction as a series of consecutive ones Sequence of objects has corresponding recording sequences, each recording sequence being distributed uniformly over a likewise predetermined step length, such that each distance between two objects corresponds to a fraction of a step length which results when the same is divided by the number of objects in a sequence.
- the device is expediently provided with endless chains as a transport device, on which carrier plates are arranged one behind the other, each of which has a number of adjacent, uniform receptacles, the inventive arrangement of different carrier plates, each associated with a specific object shape, corresponding to the predetermined sequence of objects.
- a receiving plate for one container shape and size follows another on the endless chains for another container plate for another container shape and size, be it now larger or smaller than the former container shape or container size.
- mounting plates for the first containers alternate with mounting plates for the second containers. Since this successive arrangement of different receiving plates, each assigned to a specific container shape and size, corresponds to the predetermined container sequence, with each container sequence and the recording sequence being evenly distributed over the predetermined step length, the distance between the first and second containers described corresponds to half a step length, namely that Stride length divided by two, namely the number of containers.
- stride length corresponds to two container distances.
- the predetermined step or feed length ensures that only receiving plates with these first containers are fed to the respective workstations of the device, the second containers arranged in between associated recording plates run empty on the other hand.
- the device according to the invention is now to be converted to the second container, then it is only necessary to adjust the drive by a container distance or half a step or feed length, such that the receiving plates assigned to the second containers are now each at the work stations, namely the unstacking station, the filling station, the lid placement station, the sealing or sealing station, the labeling station and the removal station. If the machine then starts up again, it is ensured that only containers of the second type in terms of shape and size are used in the step-by-step operation.
- the clock drive for adjusting the position of the transport device or endless chains with the receiving plates relative to the stations has a latching coupling which allows the above-mentioned setting of the transport device or the endless chains in the rest position of the device, such that during operation of the device the respective Feeding steps of the transport device only take the receptacles of one and the same container shape to the stations Bring in use, when changing the locking coupling when the operation of the device is interrupted, however, the receptacles of the other container shape or size.
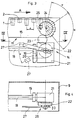
- the exemplary embodiment shown is a filling system for receiving containers 1, 2 from an unstacking station 3 and for feeding them to a filling station 4, a lid placement station 5, a closing station 6, in which the lids placed in the placement station 5 are sealed, a labeling station 7 and a removal station 8.
- These stations are arranged on a base frame 9, which rests on the floor 10 and on which a transport device 11 with receptacles 12, 13 (FIG. 2) is provided for the containers 1, 2, which are arranged in succession in the transport direction A. and the shape of the containers 1, 2 are adapted.
- a clock drive 14 is provided, which ensures a gradual advance of the transport device 11 by the same step lengths S.
- the transport device consists of two chains 15, of which only one can be seen in FIG. 1, since the second lies congruently behind it.
- Receiving plates 16, 17 are arranged on this chain, as the detail shown in FIG. 2 shows.
- These two mounting plates 16 and 17 are each adapted to two containers 1 and 2 which are different in shape and size, such that the mounting 12, 13 already mentioned above, as mentioned, have a corresponding shape.
- the containers 1 are round (FIG. 2) and longer (FIG. 1) than the containers 2, which are square and are shorter.
- the function of the device according to FIG. 1 is such that only the containers 1 are used; the containers 2 would pass through in the direction of transport A and might fall downward on the return path of the transport device in the direction of the arrow B; they have only been drawn in for clarification in FIG. 1. Under actual conditions, however, the receiving plates 16 remain empty, only the receiving plates 17 are loaded with containers 1 at the unstacking station 3.
- a container sequence consists of the two containers 1 and 2, which is distributed uniformly over the predetermined step length S, such that each distance s between two containers 1 and 2 corresponds to the fraction of the step length S which is obtained by dividing this step length S is the number of containers in a sequence, this number being two in the present case.
- the container distance s is therefore S / 2 (Fig. 1).
- FIG. 2 the containers 1 and 2 have been omitted in order to show the receptacles 12, 13 themselves.
- the clock drive 14 can be seen more clearly from FIG.
- a shaft 18 is driven by a motor (not shown) and drives a step gear 21 via a gear pair 19, 20, which via a driven gear 22, a pinion 23 and a gear 25 seated on a merely indicated shaft 24 of the transport device 11 Chains 15 drives gradually.
- the clock drive 14 has a locking clutch 26 for adapting the position of the transport device 11 or the endless chains 15 relative to the stations 3 to 8, which are not shown in FIG. 3.
- This container path s corresponds to the angular path w in FIG. 3.
- the step length S or the feed during operation of the device corresponds to the angular path W.
- a container or receiving sequence can also have more than two containers or receptacles per step length S or feed, it should be pointed out that the device can be used advantageously wherever objects, workpieces or the like are picked up and along a transport route, whether linear or circular, should be fed to successive machining or processing stations, specifically different objects or workpieces.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Supplying Of Containers To The Packaging Station (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE3814650A DE3814650C1 (cg-RX-API-DMAC7.html) | 1988-04-29 | 1988-04-29 | |
| DE3814650 | 1988-04-29 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0339297A1 EP0339297A1 (de) | 1989-11-02 |
| EP0339297B1 true EP0339297B1 (de) | 1992-01-08 |
Family
ID=6353260
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89105774A Expired - Lifetime EP0339297B1 (de) | 1988-04-29 | 1989-04-01 | Vorrichtung zum Aufnehmen von Gegenständen und zum Zuführen derselben zu längs eines Transportweges angeordneten, aufeinanderfolgenden Be- oder Verarbeitungsstationen |
| EP89904063A Pending EP0412972A1 (de) | 1988-04-29 | 1989-04-01 | Vorrichtung zum aufnehmen von gegenständen und zum zuführen derselben zu längs eines transportweges angeordneten, aufeinanderfolgenden be- oder verarbeitungsstationen |
Family Applications After (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP89904063A Pending EP0412972A1 (de) | 1988-04-29 | 1989-04-01 | Vorrichtung zum aufnehmen von gegenständen und zum zuführen derselben zu längs eines transportweges angeordneten, aufeinanderfolgenden be- oder verarbeitungsstationen |
Country Status (4)
| Country | Link |
|---|---|
| EP (2) | EP0339297B1 (cg-RX-API-DMAC7.html) |
| DE (1) | DE3814650C1 (cg-RX-API-DMAC7.html) |
| DK (1) | DK255490A (cg-RX-API-DMAC7.html) |
| WO (1) | WO1989010305A1 (cg-RX-API-DMAC7.html) |
Families Citing this family (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE9200716U1 (de) * | 1992-01-22 | 1992-05-27 | Kaak Metaalwarenfabriek B.V., Terborg | Fülltransporteinrichtung in einer Fertigungsstraße zur Fertigung von Teigprodukten |
| GB2337742A (en) * | 1996-01-04 | 1999-12-01 | Mars Uk Ltd | A method of processing a plurality of containers |
| DE10065591B4 (de) | 2000-12-28 | 2005-04-28 | Tetra Laval Holdings & Finance | Vorrichtung zum sterilen Befüllen von flaschenförmigen Packungen |
| DE102006001856A1 (de) * | 2006-01-13 | 2007-07-26 | Roland Lupper | Fehlererkennung und Fehlereingrenzung bei Abfüll-/Produktionsanlagen durch fortlaufende statistische Überwachung der Produktfehlerrate |
| CN108275324A (zh) * | 2018-03-21 | 2018-07-13 | 上海韬林机械有限公司 | 一种直列式封口灌装机及其控制方法 |
Family Cites Families (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE3618971C1 (en) * | 1986-06-05 | 1987-04-09 | Benz & Hilgers Gmbh | Apparatus for changing elongate container cells in a container-filling machine for foodstuffs and semi-luxuries |
-
1988
- 1988-04-29 DE DE3814650A patent/DE3814650C1/de not_active Expired
-
1989
- 1989-04-01 WO PCT/EP1989/000351 patent/WO1989010305A1/de not_active Ceased
- 1989-04-01 EP EP89105774A patent/EP0339297B1/de not_active Expired - Lifetime
- 1989-04-01 EP EP89904063A patent/EP0412972A1/de active Pending
-
1990
- 1990-10-23 DK DK255490A patent/DK255490A/da not_active Application Discontinuation
Also Published As
| Publication number | Publication date |
|---|---|
| WO1989010305A1 (fr) | 1989-11-02 |
| EP0412972A1 (de) | 1991-02-20 |
| EP0339297A1 (de) | 1989-11-02 |
| DK255490D0 (da) | 1990-10-23 |
| DE3814650C1 (cg-RX-API-DMAC7.html) | 1989-04-27 |
| DK255490A (da) | 1990-10-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE3151316C2 (de) | Handhabungssystem für Werkstücke | |
| DE3035191C2 (cg-RX-API-DMAC7.html) | ||
| DE69717172T2 (de) | Tragvorrichtung zum tragen von gegenständen und system mit einer solchen tragvorrichtung | |
| DE19933355C1 (de) | Verfahren zum Stapeln von Behältern aus thermoplastischem Kunststoff und Vorrichtung zur Durchführung des Verfahrens | |
| EP0569689A2 (de) | Verfahren und Vorrichtung zum Sortieren von Flaschen | |
| DE102022102079A1 (de) | Transportvorrichtung und Transportsystem für Behälter und Verarbeitungsmaschine zum Verarbeiten von Behältern | |
| EP3056440A1 (de) | Objektträger und Verpackungsanlage | |
| DE3538993C1 (en) | Apparatus for automatically exchanging cellular sheets in container-filling machines | |
| DE3814650C1 (cg-RX-API-DMAC7.html) | ||
| DE3902935A1 (de) | Brueckentellerstanzmaschine | |
| DE102019107077A1 (de) | Förderanlage zum Umsetzen zumindest eines plattenförmigen Werkstücks | |
| EP0257438A1 (de) | Vorrichtung zum Ausrichten und Anordnen von Packstücken | |
| DE69202096T2 (de) | Förderer zum Transportieren von Behältern. | |
| DE3618971C1 (en) | Apparatus for changing elongate container cells in a container-filling machine for foodstuffs and semi-luxuries | |
| CH674841A5 (cg-RX-API-DMAC7.html) | ||
| DE69117328T2 (de) | Vorrichtung zum Anbringen von Identifizierungsabschnitten an Flaschenkästen | |
| DE10145542A1 (de) | Vorrichtung zur Herstellung palettierfähiger Lagen | |
| DE8805708U1 (de) | Vorrichtung zum Aufnehmen von Gegenständen und zum Zuführen derselben zu längs eines Transportweges angeordneten, aufeinanderfolgenden Be- oder Verarbeitungsstationen | |
| CH678935A5 (en) | Filling and packing machine - has indexing conveyor in interchangeable sections for vessels of different sizes | |
| EP0195844B1 (de) | Vorrichtung, Anlage und Verfahren zum Lagern, Transportieren und Umschlagen von zylinderförmigen Materialteilen | |
| DE102016213310A1 (de) | Verpackungsanlage | |
| DE2250682B2 (de) | Vorrichtung zum Einbringen von Gegenständen in einen Verpackungskarton | |
| DE10302953B4 (de) | Abladeanordnung und Verfahren zum sortierten Abladen von in Format und/oder Aufdruck unterschiedlicher Lagen aus blattförmigen Materialien | |
| EP0384281A1 (de) | Vorrichtung zum Stapeln von Beuteln auf Bügel | |
| DE2438812A1 (de) | Vorrichtung zum selbsttaetigen befoerdern eines zu bearbeitenden gegenstandes zwischen zwei werkzeugmaschinen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): ES |
|
| 17P | Request for examination filed |
Effective date: 19900216 |
|
| XX | Miscellaneous (additional remarks) |
Free format text: VERBUNDEN MIT 89904063.8/0412972 (EUROPAEISCHE ANMELDENUMMER/VEROEFFENTLICHUNGSNUMMER) DURCH ENTSCHEIDUNG VOM 02.05.91. |
|
| 17Q | First examination report despatched |
Effective date: 19910614 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): ES FR GB IT |
|
| XX | Miscellaneous (additional remarks) |
Free format text: VERBUNDEN MIT 89904063.8/0412972 (EUROPAEISCHE ANMELDENUMMER/VEROEFFENTLICHUNGSNUMMER) DURCH ENTSCHEIDUNG VOM 02.05.91. |
|
| ITF | It: translation for a ep patent filed | ||
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) | ||
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19930430 Year of fee payment: 5 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 19940321 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19940402 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19940421 Year of fee payment: 6 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Effective date: 19950401 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19950401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19951229 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20010910 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050401 |