CN217618201U - Gear grinding machining clamp - Google Patents
Gear grinding machining clamp Download PDFInfo
- Publication number
- CN217618201U CN217618201U CN202221679381.7U CN202221679381U CN217618201U CN 217618201 U CN217618201 U CN 217618201U CN 202221679381 U CN202221679381 U CN 202221679381U CN 217618201 U CN217618201 U CN 217618201U
- Authority
- CN
- China
- Prior art keywords
- expansion
- cylindrical cylinder
- hole
- gear
- sleeve
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Landscapes
- Jigs For Machine Tools (AREA)
Abstract
本实用新型公开一种齿轮磨齿加工夹具,包括同轴设置的涨套座和涨套芯轴,涨套座包括竖直布置的圆柱筒,圆柱筒中心的涨套孔上端开口,圆柱筒的筒壁上设置有多个竖直延伸的涨开缝,以将圆柱筒筒壁的上部分割为上端分开且下端相连的多个侧壁,圆柱筒上端伸入待加工齿轮的内孔,圆柱筒下端外周设置有定位平台,定位平台上端面支撑待加工齿轮下端面,涨套芯轴能够由上端开口插入涨套孔,将圆柱筒的多个侧壁向外撑开,以使圆柱筒筒壁外侧撑紧待加工齿轮的内孔壁。通过涨套座和涨套芯轴配合撑紧待加工齿轮,方法通用性强,定位精度高,锁紧快速,固紧后就可以实现零件与装夹机构同心,可保零件加工高质量,提高效率、可靠性,方便快捷,劳动强度低。
The utility model discloses a gear grinding processing jig, which comprises an expansion sleeve seat and an expansion sleeve mandrel arranged coaxially. The expansion sleeve seat comprises a vertically arranged cylindrical cylinder, an expansion sleeve hole in the center of the cylindrical cylinder is open at the upper end, and the cylindrical cylinder has an open upper end. A plurality of vertically extending expansion slits are arranged on the cylinder wall to divide the upper part of the cylindrical cylinder wall into a plurality of side walls with the upper ends separated and the lower ends connected, and the upper end of the cylindrical cylinder extends into the inner hole of the gear to be processed, The outer periphery of the lower end is provided with a positioning platform, the upper end surface of the positioning platform supports the lower end surface of the gear to be processed, and the sleeve expansion mandrel can be inserted into the expansion sleeve hole through the opening at the upper end, and the multiple side walls of the cylindrical cylinder are stretched outward, so that the cylindrical cylinder wall The outer side supports the inner hole wall of the gear to be processed. The gear to be processed is supported by the sleeve expansion seat and the sleeve expansion mandrel. The method has strong versatility, high positioning accuracy, and fast locking. After tightening, the parts and the clamping mechanism can be concentric, which can ensure the high quality of parts processing and improve the Efficiency, reliability, convenience, and low labor intensity.
Description
技术领域technical field
本实用新型涉及零件加工领域,特别是涉及一种齿轮磨齿加工夹具。The utility model relates to the field of parts processing, in particular to a gear grinding processing fixture.
背景技术Background technique
齿轮类零件精度要求较高,齿部磨齿时,端面没有螺孔,或其他孔用于装夹时,若借助齿轮内孔装夹,则无法通过找正内孔来实现零件的找正,进行齿部的精加工,因此,进行齿部精加工,一般需要借助外部工装进行装夹来实现。此类零件加工,现有方法一般为:制作芯轴,将芯轴与齿轮组装在一起,利用芯轴的中心孔,卡盘夹持芯轴一端外圆,顶尖顶另一端中心孔实现零件的加工。Gear parts have high precision requirements. When the teeth are ground, there is no screw hole on the end face, or when other holes are used for clamping, if the inner hole of the gear is used for clamping, the alignment of the parts cannot be achieved by aligning the inner hole. The finishing of the teeth is performed. Therefore, the finishing of the teeth is generally realized by clamping with the aid of an external tool. The existing methods for processing such parts are generally: making a mandrel, assembling the mandrel and the gear together, using the center hole of the mandrel, the chuck clamps the outer circle of one end of the mandrel, and the center hole at the other end of the top of the top realizes the parts processing.
但是,现有技术中上述定位方式在安装找正过程中耗时较长,且芯轴拆卸过程中,齿轮零件内孔经常出现拉伤,严重影响表面质量,甚至造成不合格品的产生。However, in the prior art, the above-mentioned positioning method takes a long time in the process of installation and alignment, and during the disassembly of the mandrel, the inner hole of the gear part is often strained, which seriously affects the surface quality and even causes the generation of substandard products.
因此,如何提供一种方便快捷的齿轮磨齿加工夹具是本领域技术人员目前需要解决的技术问题。Therefore, how to provide a convenient and fast gear grinding jig is a technical problem that those skilled in the art need to solve at present.
实用新型内容Utility model content
本实用新型的目的是提供一种齿轮磨齿加工夹具,适合大批量的高精度零件装夹,可保零件加工高质量,提高效率、可靠性,方便快捷,劳动强度低。The purpose of the utility model is to provide a gear grinding processing fixture, which is suitable for clamping high-precision parts in large quantities, can ensure high quality of parts processing, improve efficiency, reliability, convenience and speed, and low labor intensity.
为解决上述技术问题,本实用新型提供一种齿轮磨齿加工夹具,包括同轴设置的涨套座和涨套芯轴,所述涨套座包括竖直布置的圆柱筒,所述圆柱筒中心的涨套孔上端开口,所述圆柱筒的筒壁上设置有多个竖直延伸的涨开缝,以将所述圆柱筒筒壁的上部分割为上端分开且下端相连的多个侧壁,所述圆柱筒上端伸入待加工齿轮的内孔,所述圆柱筒下端外周设置有定位平台,所述定位平台上端面支撑待加工齿轮下端面,所述涨套芯轴能够由上端开口插入所述涨套孔,将所述圆柱筒的多个侧壁向外撑开,以使所述圆柱筒筒壁外侧撑紧待加工齿轮的内孔壁。In order to solve the above technical problems, the present utility model provides a gear grinding jig, which includes a coaxially arranged expansion sleeve seat and an expansion sleeve mandrel, the expansion sleeve seat includes a vertically arranged cylindrical cylinder, and the center of the cylindrical cylinder is The upper end of the expansion sleeve hole is open, and the cylinder wall of the cylindrical cylinder is provided with a plurality of vertically extending expansion slits to divide the upper part of the cylindrical cylinder wall into a plurality of side walls with the upper ends separated and the lower ends connected, The upper end of the cylindrical cylinder extends into the inner hole of the gear to be processed, the outer periphery of the lower end of the cylindrical cylinder is provided with a positioning platform, the upper end surface of the positioning platform supports the lower end surface of the gear to be processed, and the expansion sleeve can be inserted through the opening of the upper end. The expanding sleeve hole stretches the plurality of side walls of the cylindrical cylinder outwards, so that the outer side of the cylindrical cylinder wall can support the inner hole wall of the gear to be processed.
优选地,多个所述涨开缝沿圆周均匀分布。Preferably, a plurality of the expansion slits are evenly distributed along the circumference.
优选地,所述涨开缝下端设置有减应孔。Preferably, the lower end of the expansion slit is provided with a strain relief hole.
优选地,所述圆柱筒下端设置有连通所述涨套孔的直孔,所述涨套孔的直径小于所述直孔的直径,所述直孔与所述涨套孔连接处设置有过渡圆角。Preferably, the lower end of the cylindrical cylinder is provided with a straight hole that communicates with the expansion hole, the diameter of the expansion hole is smaller than the diameter of the straight hole, and the connection between the straight hole and the expansion hole is provided with a transition rounded corners.
优选地,所述定位平台具体为围绕所述圆柱筒下端的圆环平台,所述圆环平台下端面与所述圆柱筒下端面平齐。Preferably, the positioning platform is an annular platform surrounding the lower end of the cylindrical cylinder, and the lower end surface of the annular platform is flush with the lower end surface of the cylindrical cylinder.
优选地,所述定位平台上设置有多个阶梯通孔,通过螺栓穿过所述阶梯通孔连接工作台。Preferably, the positioning platform is provided with a plurality of stepped through holes, and bolts pass through the stepped through holes to connect the workbench.
优选地,所述圆柱筒和所述定位平台一体式成型。Preferably, the cylindrical barrel and the positioning platform are integrally formed.
优选地,所述涨套芯轴直径由上至下逐渐变小,所述涨套芯轴外壁锥度与涨套孔锥度配合。Preferably, the diameter of the sleeve-expanding mandrel gradually decreases from top to bottom, and the taper of the outer wall of the sleeve-expanding mandrel matches the taper of the sleeve-expanding hole.
优选地,所述涨套芯轴上端设置有吊环。Preferably, the upper end of the expansion sleeve is provided with a lifting ring.
优选地,所述涨套芯轴上端面中心处设置有螺纹孔,所述吊环下端拧入所述螺纹孔内。Preferably, a threaded hole is provided at the center of the upper end face of the expanding mandrel, and the lower end of the lifting ring is screwed into the threaded hole.
本实用新型提供一种齿轮磨齿加工夹具,包括同轴设置的涨套座和涨套芯轴,涨套座包括竖直布置的圆柱筒,圆柱筒中心的涨套孔上端开口,圆柱筒的筒壁上设置有多个竖直延伸的涨开缝,以将圆柱筒筒壁的上部分割为上端分开且下端相连的多个侧壁,圆柱筒上端伸入待加工齿轮的内孔,圆柱筒下端外周设置有定位平台,定位平台上端面支撑待加工齿轮下端面,涨套芯轴能够由上端开口插入涨套孔,将圆柱筒的多个侧壁向外撑开,以使圆柱筒筒壁外侧撑紧待加工齿轮的内孔壁。The utility model provides a gear grinding processing jig, which comprises an expansion sleeve seat and an expansion sleeve core shaft arranged coaxially, the expansion sleeve seat comprises a vertically arranged cylindrical cylinder, an expansion sleeve hole in the center of the cylindrical cylinder is open at the upper end, A plurality of vertically extending expansion slits are arranged on the cylinder wall to divide the upper part of the cylindrical cylinder wall into a plurality of side walls with the upper ends separated and the lower ends connected, and the upper end of the cylindrical cylinder extends into the inner hole of the gear to be processed, The outer periphery of the lower end is provided with a positioning platform, the upper end surface of the positioning platform supports the lower end surface of the gear to be processed, and the sleeve expansion mandrel can be inserted into the expansion sleeve hole through the opening at the upper end, and the multiple side walls of the cylindrical cylinder are stretched outward, so that the cylindrical cylinder wall The outer side supports the inner hole wall of the gear to be processed.
通过涨套座和涨套芯轴配合撑紧待加工齿轮,方法通用性强,定位精度高,锁紧快速,固紧后就可以实现零件与装夹机构同心,无需再次找正,适合大批量的高精度零件装夹,可保零件加工高质量,提高效率、可靠性,方便快捷,劳动强度低。The gear to be processed is supported by the sleeve expansion seat and the sleeve expansion mandrel. The method has strong versatility, high positioning accuracy, and fast locking. After tightening, the parts and the clamping mechanism can be concentric, and there is no need to align again, which is suitable for large quantities. High-precision parts clamping can ensure high-quality parts processing, improve efficiency, reliability, convenience, and low labor intensity.
附图说明Description of drawings
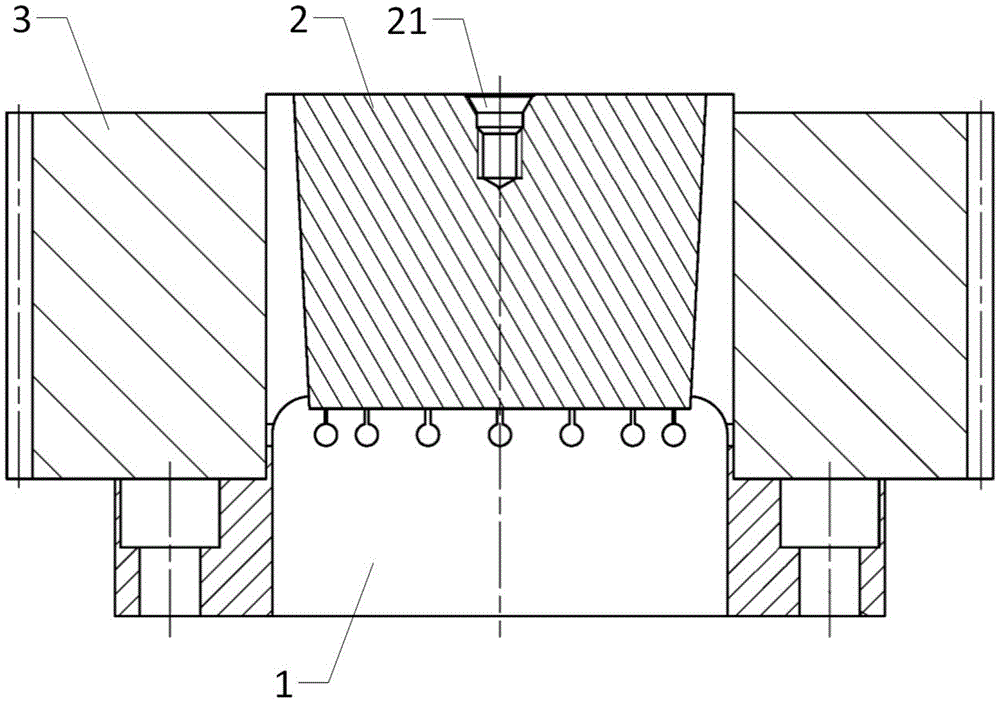
图1为本实用新型所提供的齿轮磨齿加工夹具的一种具体实施方式的剖面示意图;1 is a schematic cross-sectional view of a specific embodiment of a gear grinding processing fixture provided by the utility model;
图2为本实用新型所提供的齿轮磨齿加工夹具的一种具体实施方式中涨套座的主视剖面示意图;Fig. 2 is the front sectional schematic diagram of the expansion sleeve seat in a specific embodiment of the gear grinding processing fixture provided by the utility model;
图3为本实用新型所提供的齿轮磨齿加工夹具的一种具体实施方式中涨套座的俯视示意图。FIG. 3 is a schematic top view of the expansion sleeve seat in a specific embodiment of the gear grinding processing fixture provided by the present invention.
具体实施方式Detailed ways
本实用新型的核心是提供一种齿轮磨齿加工夹具,适合大批量的高精度零件装夹,可保零件加工高质量,提高效率、可靠性,方便快捷,劳动强度低。The core of the utility model is to provide a gear grinding processing fixture, which is suitable for clamping high-precision parts in large quantities, and can ensure the high quality of parts processing, improve efficiency, reliability, convenience and speed, and low labor intensity.
为了使本技术领域的人员更好地理解本实用新型方案,下面结合附图和具体实施方式对本实用新型作进一步的详细说明。In order to make those skilled in the art better understand the solution of the present invention, the present invention will be further described in detail below with reference to the accompanying drawings and specific embodiments.
请参考图1至图3,图1为本实用新型所提供的齿轮磨齿加工夹具的一种具体实施方式的剖面示意图;图2为本实用新型所提供的齿轮磨齿加工夹具的一种具体实施方式中涨套座的主视剖面示意图;图3为本实用新型所提供的齿轮磨齿加工夹具的一种具体实施方式中涨套座的俯视示意图。Please refer to FIGS. 1 to 3 , FIG. 1 is a schematic cross-sectional view of a specific embodiment of a gear grinding jig provided by the utility model; FIG. 2 is a specific embodiment of the gear grinding jig provided by the utility model. Figure 3 is a schematic top view of the expansion sleeve in a specific embodiment of the gear grinding processing fixture provided by the utility model.
本实用新型具体实施方式提供一种齿轮磨齿加工夹具,包括同轴设置的涨套座1和涨套芯轴2,涨套座1包括竖直布置的圆柱筒11,圆柱筒11中心设置有涨套孔,涨套孔上端开口,圆柱筒11的筒壁上设置有多个竖直延伸的涨开缝12,涨开缝12由筒壁顶端向下切割至筒壁中部,多个涨开缝12沿圆周方向依次排列,通过多个涨开缝12,将圆柱筒11筒壁的上部分割为多个侧壁,多个侧壁围绕轴心依次排列形成筒形结构。多个侧壁的上端分开且下端相连,圆柱筒11上端伸入待加工齿轮3的内孔,圆柱筒11下端外周设置有定位平台13,通过定位平台13安装于工作台,定位平台13上端面支撑待加工齿轮3下端面,涨套芯轴2能够由上端开口插入涨套孔,将圆柱筒11的多个侧壁向外撑开,以使圆柱筒11筒壁外侧撑紧待加工齿轮3的内孔壁。The specific embodiment of the present utility model provides a gear grinding jig, which includes an expanding
通过涨套座1和涨套芯轴2配合撑紧待加工齿轮3,方法通用性强,定位精度高,锁紧快速,固紧后就可以实现零件与装夹机构同心,无需再次找正,适合大批量的高精度零件装夹,可保零件加工高质量,提高效率、可靠性,方便快捷,劳动强度低。The
具体地,定位平台13具体为围绕圆柱筒11下端的圆环平台,圆环平台下端面与圆柱筒11下端面平齐。Specifically, the
使用过程中,将涨套座1放置在工作台上,找正涨套座1外圆,保证涨套座1上下两处外圆同轴度,找正下端面,保证与外圆垂直度,然后将涨套座1固紧在工作台上。保证涨套座1与机床工作台同心且不能出现相对移动,具体地各外表面的粗糙度保证Ra0.8。During use, place the
将待加工齿轮3安装在圆柱筒11上端,将待加工齿轮3内孔与圆柱筒11筒壁外侧配合,待加工齿轮3下端面与定位平台13上端面配合。Install the
将涨套芯轴2由上端开口插入涨套孔内,向下压紧涨套芯轴2,由于涨开缝12的结构可以产生径向弹性伸缩量,通过压紧涨套芯轴2就可以圆柱筒11筒壁向外张开,使圆柱筒11径向变大,撑紧待加工齿轮3的内孔壁,各部件之间实现过盈配合,即可锁紧零件,实现涨套座1、待加工齿轮3、涨套芯轴2三者的精确定位。Insert the
完成装夹,进行齿部精加工,不同工件重复定位精度可达到0.01,磨齿精度可达三级。After completing the clamping and finishing the teeth, the repeated positioning accuracy of different workpieces can reach 0.01, and the grinding accuracy can reach three levels.
完成齿轮齿部精加工,将涨套芯轴2拉出,在弹性作用下,圆柱筒11筒壁向内收回,涨套座1外圆与待加工齿轮3内孔变为间隙配合,可轻松拆下待加工齿轮3,不会对齿轮内孔产生损伤。After finishing the finishing of the gear teeth, pull out the
采用上述方法,通过涨套座1、涨套芯轴2、待加工齿轮3的装配,固紧后就可以实现零件与装夹机构定位,无需再次对工件进行找正,大大提高了工作效率和定位精度。零件内孔直径变化在±0.1范围内,涨套座1都可装夹。增加变径套、调整垫,可以装夹多种不同直径、不同齿宽的零件。By adopting the above method, through the assembly of the
优选地,多个涨开缝12沿圆周均匀分布。涨开缝12下端设置有减应孔14,避免部件开裂,保证设备安全可靠。Preferably, the plurality of
在本实用新型具体实施方式提供的齿轮磨齿加工夹具中,圆柱筒11为上下贯穿的套筒结构,圆柱筒11下端设置有连通涨套孔的直孔,涨套孔的直径小于直孔的直径,直孔与涨套孔连接处设置有过渡圆角,使连接处筒壁较薄,便于侧壁的弹性变形。In the gear grinding processing fixture provided by the specific embodiment of the present invention, the
为了实现与工作台的稳定连接,定位平台13上设置有多个阶梯通孔15,安装时,螺栓穿过阶梯通孔15后连接工作台,且螺栓完全埋入阶梯通孔15内,保证定位平台13上端面平面度。具体地,多个阶梯通孔15沿圆周方向依次均匀排布在定位平台13上,也可采用其他连接方式,如卡扣连接等,均在本实用新型的保护范围之内。其中,圆柱筒11和定位平台13一体式成型。In order to achieve stable connection with the workbench, the
为了便于涨套芯轴2的顺利拔出,可在涨套芯轴2外周设置倒锥面,同时涨套孔内壁也设置成匹配的锥面,即涨套芯轴2呈倒立的圆台形,涨套芯轴2直径由上至下逐渐变小,涨套孔形状相似,涨套芯轴2外壁锥度与涨套孔锥度配合。In order to facilitate the smooth pull-out of the sleeve-expanding
在上述各具体实施方式提供的齿轮磨齿加工夹具的基础上,涨套芯轴2上端设置有吊环。具体地,涨套芯轴2上端面中心处设置有螺纹孔21,吊环下端拧入螺纹孔21内。完成齿轮齿部精加工,将吊环拧入涨套芯轴2上端面的螺纹孔21中,即可将涨套芯轴2拉出。On the basis of the gear grinding processing jig provided by the above-mentioned specific embodiments, the upper end of the expanding
以上对本实用新型所提供的齿轮磨齿加工夹具进行了详细介绍。本文中应用了具体个例对本实用新型的原理及实施方式进行了阐述,以上实施例的说明只是用于帮助理解本实用新型的方法及其核心思想。应当指出,对于本技术领域的普通技术人员来说,在不脱离本实用新型原理的前提下,还可以对本实用新型进行若干改进和修饰,这些改进和修饰也落入本实用新型权利要求的保护范围内。The gear grinding processing fixture provided by the present utility model has been introduced in detail above. The principles and implementations of the present invention are described herein by using specific examples, and the descriptions of the above embodiments are only used to help understand the method and the core idea of the present invention. It should be pointed out that for those of ordinary skill in the art, without departing from the principles of the present utility model, some improvements and modifications can also be made to the present utility model, and these improvements and modifications also fall into the protection of the claims of the present utility model. within the range.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221679381.7U CN217618201U (en) | 2022-07-01 | 2022-07-01 | Gear grinding machining clamp |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221679381.7U CN217618201U (en) | 2022-07-01 | 2022-07-01 | Gear grinding machining clamp |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN217618201U true CN217618201U (en) | 2022-10-21 |
Family
ID=83631191
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202221679381.7U Active CN217618201U (en) | 2022-07-01 | 2022-07-01 | Gear grinding machining clamp |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN217618201U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115922373A (en) * | 2022-12-12 | 2023-04-07 | 陕西渭河工模具有限公司 | A processing tool and method for a ring-shaped flexible spline |
-
2022
- 2022-07-01 CN CN202221679381.7U patent/CN217618201U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115922373A (en) * | 2022-12-12 | 2023-04-07 | 陕西渭河工模具有限公司 | A processing tool and method for a ring-shaped flexible spline |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN207414845U (en) | A kind of numerically-controlled machine tool fast-assembling precise clamp | |
| CN217254691U (en) | High-precision inner gear pitch circle inner tensioning rubber expansion sleeve and gear clamp | |
| CN108481057B (en) | Fixtures for Turning Ball Shaft Parts | |
| CN205816856U (en) | A kind of Wedge-type multiple operation general automation fixture | |
| CN115971918A (en) | Tooling fixture and processing method for porous processing of thin-walled shell | |
| CN112091248B (en) | Turning clamping device and clamping method for pointed cone-shaped part | |
| CN110625201A (en) | Shaft gear shaping clamp | |
| CN106346286A (en) | Sphere type part turning installing and clamping tooling | |
| CN207668907U (en) | A kind of fixture with taper hole workpiece for numerically-controlled machine tool | |
| CN108481192A (en) | A kind of mill fixture and clamping method suitable for the long spacer of thin-walled | |
| CN111203603B (en) | Interchange clamping device for turbine disc | |
| CN208575540U (en) | A kind of device having both axial fast precise, radial direction centering and clamping function | |
| CN110000579A (en) | A kind of the centrifugal impeller batch numerical control Special Fixture for Machining and installation method of center non through hole | |
| CN110842616B (en) | A clamping tool for machining gear shaft | |
| CN110961960B (en) | Numerical control lathe clamp for machining slender shaft with flange plate | |
| CN112846881A (en) | Clamp for processing arc surface of workpiece and processing method | |
| CN216325193U (en) | Universal clamp for bidirectional machining of scroll plate | |
| CN203804343U (en) | Self-centering tool clamp used for hobbing worm wheel | |
| CN211135550U (en) | Cutter fixing device of numerical control deep hole drilling and milling machine | |
| KR100563589B1 (en) | Hydraulic collet chuck assembly for eccentric machining | |
| CN111804957A (en) | Fixing device for drilling equal-division hole plate | |
| CN206253943U (en) | A kind of taper hole hollow shaft clamping device for processing | |
| CN107283013B (en) | It is a kind of for processing the positioning indexing means and processing method of oil well cutting ferrule | |
| CN216503559U (en) | Self-centering clamp for machining motor stator casing | |
| CN209125592U (en) | Thin-wall gear fixture for grinding inner holes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |