CN211052191U - An automatic centering fixture - Google Patents
An automatic centering fixture Download PDFInfo
- Publication number
- CN211052191U CN211052191U CN201921750152.8U CN201921750152U CN211052191U CN 211052191 U CN211052191 U CN 211052191U CN 201921750152 U CN201921750152 U CN 201921750152U CN 211052191 U CN211052191 U CN 211052191U
- Authority
- CN
- China
- Prior art keywords
- base
- clamping
- wedge
- automatic centering
- workpiece
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Jigs For Machine Tools (AREA)
Abstract
本实用新型提供了一种自动找中心夹具,包括底座、X向挡块、Y向夹紧组件和Z向压紧组件,X向挡块固设在所述底座的一端,Z向压紧组件设置在底座上,Y向夹紧组件包括浮动推销、弹性部和设置在浮动推销两侧的夹块。通过弹性部驱使浮动推销下降,使得楔形孔变大,使得两个夹块相互靠近。当工件放置到两夹块之间时,两夹块被撑开,楔形孔变小,浮动推销被抬起,同时两个夹块之间的预紧力始终将工件夹紧并向中心靠拢,实现工件的自动找中心。随后将工件的一端抵顶X向挡块,并用Z向压紧组件将工件压紧,完成工件的固定。
The utility model provides an automatic centering fixture, which comprises a base, an X-direction block, a Y-direction clamping component and a Z-direction pressing component. The X-direction stopper is fixed on one end of the base, and the Z-direction pressing component Set on the base, the Y-direction clamping assembly includes a floating push pin, an elastic part and a clamping block arranged on both sides of the floating push pin. The floating push pin is driven down by the elastic part, so that the wedge-shaped hole becomes larger, so that the two clamping blocks are close to each other. When the workpiece is placed between the two clamping blocks, the two clamping blocks are opened, the wedge-shaped hole becomes smaller, the floating pusher is lifted, and the preload between the two clamping blocks always clamps the workpiece and moves closer to the center, Realize the automatic centering of the workpiece. Then push one end of the workpiece against the X-direction stopper, and use the Z-direction pressing component to compress the workpiece to complete the fixation of the workpiece.
Description
技术领域technical field
本实用新型涉及机加工领域,具体涉及一种自动找中心夹具。The utility model relates to the field of machining, in particular to an automatic centering fixture.
背景技术Background technique
在坯料(以下称为工件)的加工过程中,需要对坯料进行固定以及对中。但现有的定位夹具虽然能将工件固定,却无法准确地对正产品的中心线。During the processing of the blank (hereinafter referred to as the workpiece), the blank needs to be fixed and aligned. However, although the existing positioning fixture can fix the workpiece, it cannot accurately align the center line of the product.
如图1所示,工件100通过将两侧的定位齿101插进下方的治具200中,再用压板300从上方锁紧固定。本实用新型中的工件100为挤型材,挤型模具的尺寸是固定的,理论上其生产出的工件尺寸也是固定的。但是,挤压成型出来的工件100的两侧的定位齿101尺寸是有差异的,这种变异主要来自自热变形(即热胀冷缩)。这种变形的特点是相对尺寸同时变化(即一同变大或一同变小),工件100的中心固定,两侧尺寸宽度有变化。这样会造成工件Y方向定位尺寸的变异量大,影响定位,加工产品的位置不准确,尺寸良率低。As shown in FIG. 1 , the
实用新型内容Utility model content
本实用新型的一个目的在于提供一种能够自动找正工件中心及定位的自动找中心夹具。One object of the present utility model is to provide an automatic centering fixture capable of automatically centering and positioning the workpiece.
本实用新型解决其技术问题所采用的技术方案是,提供一种自动找中心夹具,包括底座、X向挡块、Y向夹紧组件和Z向压紧组件,所述X向挡块固设在所述底座的一端,所述Z向压紧组件设置在底座上,所述Y向夹紧组件包括:浮动推销,可升降地设置在底座中,底部呈锥形或楔形;弹性部,一端连接所述底座,另一端连接浮动推销的顶部;以及设置在浮动推销两侧的夹块,一端外伸出底座,另一端插设在底座中并设有楔形缺口;两个所述夹块通过楔形缺口的相互抱合形成楔形孔;所述浮动推销插设在所述楔形孔中;在所述浮动推销下降时,两个夹块相互靠近;在两个夹块相互远离时,所述浮动推销升起。The technical solution adopted by the utility model to solve the technical problem is to provide an automatic centering fixture, which includes a base, an X-direction block, a Y-direction clamping assembly and a Z-direction pressing assembly, and the X-direction block is fixed At one end of the base, the Z-direction pressing assembly is arranged on the base, and the Y-direction clamping assembly includes: a floating push-button, which is arranged in the base in a liftable manner, and the bottom is conical or wedge-shaped; an elastic part, one end The base is connected to the base, and the other end is connected to the top of the floating push-button; and the clamping blocks are arranged on both sides of the floating push-button, one end extends out of the base, and the other end is inserted into the base and has a wedge-shaped notch; the two clamping blocks pass through Wedge-shaped holes are formed by the wedge-shaped notches cohesion; the floating push pins are inserted into the wedge-shaped holes; when the floating push pins descend, the two clamping blocks approach each other; when the two clamping blocks move away from each other, the floating push pins rising.
本实用新型提供的一种自动找中心夹具,通过弹性部驱使浮动推销下降,使得楔形孔变大,使得两个夹块相互靠近。当工件放置到两夹块之间时,两夹块被撑开,楔形孔变小,浮动推销被抬起,同时两个夹块之间的预紧力始终将工件夹紧并向中心靠拢,实现工件的自动找中心。随后将工件的一端抵顶X 向挡块,并用Z向压紧组件将工件压紧,完成工件的固定。The automatic centering clamp provided by the utility model can drive the floating push pin to descend through the elastic part, so that the wedge-shaped hole becomes larger and the two clamping blocks are close to each other. When the workpiece is placed between the two clamping blocks, the two clamping blocks are opened, the wedge-shaped hole becomes smaller, the floating pusher is lifted, and the preload between the two clamping blocks always clamps the workpiece and moves closer to the center. Realize the automatic centering of the workpiece. Then push one end of the workpiece against the X-direction stopper, and use the Z-direction pressing component to press the workpiece to complete the fixation of the workpiece.
在一些实施方式中,每一所述夹块均包括夹持臂以及与夹持臂垂直连接的连接臂;所述楔形缺口开设在所述连接臂上;两个所述连接臂通过所述楔形缺口相互抱合,形成所述楔形孔。In some embodiments, each of the clamping blocks includes a clamping arm and a connecting arm vertically connected to the clamping arm; the wedge-shaped notch is formed on the connecting arm; the two connecting arms pass through the wedge-shaped The notches overlap each other to form the wedge-shaped hole.
在一些实施方式中,所述Y向夹紧组件还包括卡簧;所述卡簧卡接在所述夹持臂上,垂直于所述夹持臂,并抵压在底座的上表面上。In some embodiments, the Y-direction clamping assembly further includes a retaining spring; the retaining spring is clamped on the clamping arm, is perpendicular to the clamping arm, and is pressed against the upper surface of the base.
在一些实施方式中,所述夹持臂远离连接臂的一端还设有用于导向的斜坡。In some embodiments, the end of the clamping arm away from the connecting arm is further provided with a slope for guiding.
在一些实施方式中,所述弹性部为压缩弹簧;所述压缩弹簧的两端分别连接底座和浮动推销。In some embodiments, the elastic part is a compression spring; two ends of the compression spring are respectively connected to the base and the floating pusher.
在一些实施方式中,所述Y向夹紧组件还包括无头螺丝;所述无头螺丝与底座螺纹连接;所述压缩弹簧的一端抵顶无头螺丝,另一端抵压所述浮动推销。In some embodiments, the Y-direction clamping assembly further includes a headless screw; the headless screw is threadedly connected to the base; one end of the compression spring is pressed against the headless screw, and the other end is pressed against the floating push pin.
在一些实施方式中,所述Z向压紧组件包括压条和锁紧螺钉;所述压条抵压在工件上,并通过所述螺钉固定在底座上。In some embodiments, the Z-direction pressing assembly includes a pressing bar and a locking screw; the pressing bar is pressed against the workpiece and fixed on the base by the screw.
在一些实施方式中,所述底座的两端设有凸台,每一所述凸台上开设有安装孔。In some embodiments, two ends of the base are provided with bosses, and each of the bosses is provided with a mounting hole.
在一些实施方式中,所述底座的两侧还设有把手。In some embodiments, handles are also provided on both sides of the base.
附图说明Description of drawings
下面将结合附图及实施例对本实用新型作进一步说明,附图中:The utility model will be further described below in conjunction with the accompanying drawings and embodiments, in the accompanying drawings:
图1是关联技术中的定位治具的使用状态示意图;FIG. 1 is a schematic diagram of the use state of the positioning fixture in the related art;
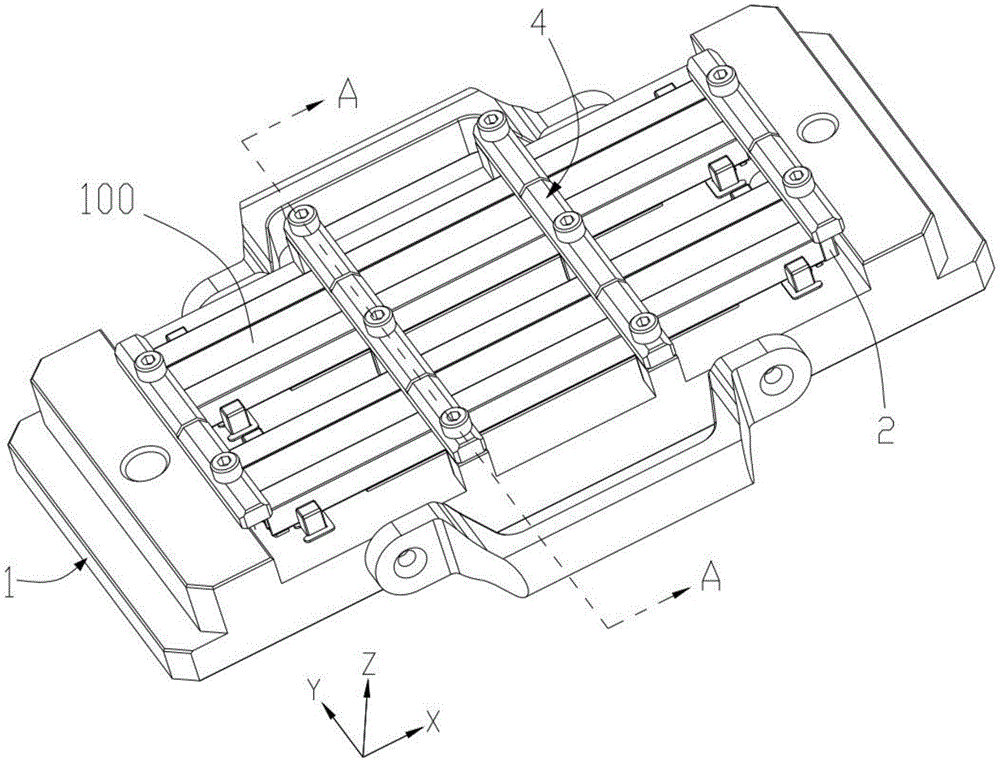
图2是本实用新型实施例的已装工件的自动找中心夹具的立体示意图;Fig. 2 is the three-dimensional schematic diagram of the automatic centering fixture of the mounted workpiece according to the embodiment of the present invention;
图3是本实用新型实施例的未装工件的自动找中心夹具的立体示意图;3 is a perspective view of an automatic centering fixture without a workpiece according to an embodiment of the present invention;
图4是本实用新型实施例的底座的立体示意图;Fig. 4 is the three-dimensional schematic diagram of the base of the embodiment of the present invention;
图5是本实用新型实施例的仰视示意图;Fig. 5 is the bottom view schematic diagram of the embodiment of the present utility model;
图6是本实用新型实施例的X向挡块的立体示意图;6 is a perspective view of an X-direction stopper according to an embodiment of the present invention;
图7是图2中A-A位置的剖面示意图;Fig. 7 is the sectional schematic diagram of A-A position among Fig. 2;
图8是本实用新型实施例的自动找中心夹具的分解示意图;Fig. 8 is the exploded schematic diagram of the automatic centering fixture of the embodiment of the present invention;
图9是本实用新型实施例的夹块的立体示意图;9 is a perspective view of a clamping block according to an embodiment of the present invention;
图10是本实用新型实施例的夹块的工作状态示意图;Fig. 10 is the working state schematic diagram of the clamping block of the embodiment of the present invention;
图11是图8中B位置的局部放大示意图。FIG. 11 is a partially enlarged schematic view of the position B in FIG. 8 .
附图标记说明如下:The reference numerals are explained as follows:
100-工件;101-定位齿;200-治具;300-压板;1-底座;11-盖板;12-凸台; 14-把手13-安装孔;2-X向挡块;31-浮动推销;32-弹性部;33-夹块;34-夹持臂;35-连接臂;36-楔形缺口;37-楔形孔;38-卡簧;39-无头螺丝;4-Z向压紧组件;41-压条;42-锁紧螺钉。100-workpiece; 101-positioning teeth; 200-jig; 300-pressing plate; 1-base; 11-cover plate; 12-boss; 14-handle 13-installation hole; 2-X-direction stop; 31-floating 32-elastic part; 33-clamping block; 34-clamping arm; 35-connecting arm; 36-wedge-shaped notch; 37-wedge-shaped hole; 38-retaining spring; 39-headless screw; Component; 41-pressing strip; 42-locking screw.
具体实施方式Detailed ways
体现本实用新型特征与优点的典型实施方式将在以下的说明中详细叙述。应理解的是本实用新型能够在不同的实施方式上具有各种的变化,其皆不脱离本实用新型的范围,且其中的说明及图示在本质上是当作说明之用,而非用以限制本实用新型。Typical embodiments embodying the features and advantages of the present invention will be described in detail in the following description. It should be understood that the present utility model can have various changes in different embodiments without departing from the scope of the present utility model, and the descriptions and illustrations therein are essentially for the purpose of illustration rather than use to limit the utility model.
参考图2、图3、图7、图8,本实施例提供一种自动找中心夹具,包括底座1、X向挡块2、Y向夹紧组件和Z向压紧组件4。Referring to FIG. 2 , FIG. 3 , FIG. 7 , and FIG. 8 , this embodiment provides an automatic centering fixture, which includes a base 1 , an
其中,X向挡块2固设在底座1的一端。Z向压紧组件4设置在底座1上,用以按压工件100。Y向夹紧组件包括浮动推销31、弹性部32以及设置在浮动推销31两侧的夹块33。浮动推销31可升降地设置在底座1中,其底部呈锥形或楔形。弹性部32的一端连接所述底座1,另一端连接浮动推销31的顶部。夹块33可滑动地设置在底座1上。夹块33的一端外伸出底座1,另一端插设在底座1中并设有楔形缺口36。两个夹块33通过楔形缺口36的相互抱合形成楔形孔37。上述浮动推销31插设在所述楔形孔37中。当浮动推销31 下降时,两个夹块33相互靠近并且两个夹块33之间的间距小于工件100的宽度;当两个夹块33相互远离时,浮动推销31升起。Wherein, the
通过弹性部32驱使浮动推销31下降,使得楔形孔37变大,使得两个夹块33相互靠近。当工件100放置到两夹块33之间时,两夹块33被撑开,楔形孔37变小,浮动推销31被抬起,同时两个夹块33之间的预紧力始终将工件100夹紧并向中心靠拢,实现工件100的自动找中心。随后将工件100的一端抵顶X向挡块2,并用Z向压紧组件4将工件100压紧,完成工件100的固定。The floating
具体地,本实施例中的自动找中心夹具为双工位夹具。Specifically, the automatic centering fixture in this embodiment is a double-station fixture.
参考图4、图5,底座1作为承载主体,其内部开设有若干容置槽,用于容置Y向夹紧组件,并以盖板11封闭。底座1的两端设有凸台12,凸台12 上开有安装孔13,通过安装孔13可以将整套夹具安装到机床的工作台上。底座1的两侧还设有把手14,便于搬运整套夹具。Referring to FIG. 4 and FIG. 5 , the base 1 is used as a bearing body, and a plurality of accommodating grooves are opened in its interior for accommodating the Y-direction clamping components, and are closed by a
参考图6,本实施例中的X向挡块2呈“7”字形。X向挡块2插设在底座1上,并以螺钉(图未示)固定。Referring to FIG. 6 , the
一同参考图9、图10,具体地,每一个夹块33均包括夹持臂34以及与夹持臂34垂直连接的连接臂35。所述楔形缺口36开设在所述连接臂35上。当楔形孔37变大时,两个连接臂35相互靠拢,两个夹持臂34也相互靠拢;当楔形孔37变小时,两个连接臂35相互远离,两个夹持臂34也相互远离。因此,通过改变楔形孔37的大小,则可控制两个夹持臂34的分开和靠拢,结构十分巧妙、便捷。Referring to FIG. 9 and FIG. 10 together, in particular, each clamping
参考图11,Y向夹紧组件还包括卡簧38。所述卡簧38卡接在所述夹持臂 34上,且垂直于夹持臂34,并抵压在底座1的上表面上。通过在夹持臂34 上设有卡簧38,而卡簧38贴近底座1的表面,当夹持臂34来回移动时,可保证夹持臂34不倾斜。Referring to FIG. 11 , the Y-direction clamping assembly further includes a retaining
继续参考图11,夹持臂34远离连接臂35的一端(即顶端)还设有用于导向的斜坡,便于工件100放进两夹持臂34之间。Continuing to refer to FIG. 11 , one end (ie, the top end) of the clamping
在本实施例中,上述弹性部32为压缩弹簧,压缩弹簧的两端分别连接底座1和浮动推销31。在其他实施例中,弹性部32也可采用两个磁铁,利用同性相斥的原理为浮动推销31提供向下的压力。进一步地,Y向夹紧组件还包括无头螺丝39。所述无头螺丝39与底座1螺纹连接。压缩弹簧被压缩在无头螺丝39与浮动推销31之间。通过在底座1的表面上装有无头螺丝39,不仅便于从夹具的上方更换压缩弹簧,无需翻转底座1,而且通过拧动无头螺丝39,可以调节无头螺丝39在底座1中的高度,进而改变压缩弹簧的长度,实现改变两夹块33之间的预紧力(即夹紧力度)。In this embodiment, the
继续参考图2、图3,Z向压紧组件4包括压条41和锁紧螺钉42。所述压条41抵压在工件100上,并通过所述螺钉固定在底座1上,十分简便快捷。在本实施例中,底座1上设有多组Z向压紧组件4。在其他实施例中,Z向压紧组件4还可以采用气缸结构,通过气缸的活塞杆的伸出,将工件100从上方压紧。Continuing to refer to FIGS. 2 and 3 , the Z-direction pressing assembly 4 includes a
综合上述对自动找中心夹具的结构描述,以下对该夹具的使用方法进行具体描述:Based on the above structural description of the automatic centering fixture, the following is a detailed description of the use method of the fixture:
将工件100按压进两夹持臂34之间,两夹持臂34被撑开,楔形孔37缩小,浮动推销31被抬升,两夹持臂34在预紧力的作用下从两侧将工件100 夹紧并对中,消除因定位齿101变异而与夹具之间的间隙,从而消除了宽度尺寸变化带来的定位影响。随后将工件100的一端抵顶X向挡块2。最终下压工件100至其定位齿101紧贴底座1表面,并通过压条41和锁紧螺钉42将工件 100固定。The
在加工完毕后,解开锁紧螺钉42和压条41,从两个夹持臂34之间取出工件100。同时压缩弹簧驱使浮动推销31下降,楔形孔37被扩大,两夹持臂 34相互靠近复位。After the processing is completed, the locking
虽然已参照上述的典型实施方式描述了本实用新型,但应当理解,所用的术语是说明和示例性、而非限制性的术语。由于本实用新型能够以多种形式具体实施而不脱离实用新型的精神或实质,所以应当理解,上述实施方式不限于任何前述的细节,而应在随附权利要求所限定的精神和范围内广泛地解释,因此落入权利要求或其等效范围内的全部变化和改型都应为随附权利要求所涵盖。While the present invention has been described with reference to the above-described exemplary embodiments, it is to be understood that the terms used are of description and illustration, and not of limitation. Since the invention can be embodied in various forms without departing from the spirit or essence of the invention, it should be understood that the above-described embodiments are not limited to any of the foregoing details, but should be broadly within the spirit and scope defined by the appended claims Therefore, all changes and modifications that come within the scope of the claims or their equivalents are intended to be covered by the appended claims.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921750152.8U CN211052191U (en) | 2019-10-18 | 2019-10-18 | An automatic centering fixture |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921750152.8U CN211052191U (en) | 2019-10-18 | 2019-10-18 | An automatic centering fixture |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211052191U true CN211052191U (en) | 2020-07-21 |
Family
ID=71588409
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921750152.8U Expired - Fee Related CN211052191U (en) | 2019-10-18 | 2019-10-18 | An automatic centering fixture |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211052191U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112536401A (en) * | 2020-11-23 | 2021-03-23 | 苏州领裕电子科技有限公司 | Wire rod riveting automation equipment |
-
2019
- 2019-10-18 CN CN201921750152.8U patent/CN211052191U/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112536401A (en) * | 2020-11-23 | 2021-03-23 | 苏州领裕电子科技有限公司 | Wire rod riveting automation equipment |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN206277164U (en) | Clamping and positioning device | |
| CN210702250U (en) | Chip pin straightening device | |
| CN215355681U (en) | Stamping die capable of synchronously punching multiple surfaces | |
| CN212419483U (en) | Cold forming device for I-shaped sleeve | |
| CN209935654U (en) | Punching machine with positioning function | |
| CN219189302U (en) | A track shoe self-positioning drilling and milling tool | |
| CN213378615U (en) | Bending equipment with quick clamping structure for production of stamping die | |
| CN214442274U (en) | Die for punching processing of plate with middle part protruding | |
| CN212190867U (en) | Side-push forming die | |
| CN109827750B (en) | An adjustable-angle workpiece fixture suitable for 3D scanning galvanometer test bench | |
| CN216097220U (en) | Multi-product part welding fixture | |
| CN223819455U (en) | Self-positioning punching tool | |
| CN216152208U (en) | Clamping seat positioning tool | |
| CN223981098U (en) | A MOS transistor preforming fixture | |
| CN217990696U (en) | Stamping die and stamping device | |
| CN224043121U (en) | Jig for clamping and positioning | |
| CN223455591U (en) | Clamp for machining special-shaped product | |
| CN216464273U (en) | Fixing device of new forms of energy mould production usefulness | |
| CN218982900U (en) | Stamping piece embeds slider formula stamping die | |
| CN221675585U (en) | Mechanical accessory stamping equipment with clamping and positioning structure | |
| CN223070985U (en) | Punching parts bracket process keyway positioning fixture | |
| CN222537615U (en) | A new type of fixture for machining mechanical equipment | |
| CN210281499U (en) | Frame multistation corner cut anchor clamps | |
| CN205362377U (en) | Leaf spring die mould piercing press | |
| CN205380472U (en) | Pile up processing of formula frozen machine helical guideway and use frock |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20200721 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |