Multi-cutter high-efficiency synchronous dynamic balance turning machine tool
Technical Field
The utility model belongs to the technical field of the machine-building, concretely relates to synchronous dynamic balance turning machine tool of multitool high efficiency.
Background
In traditional lathe work, machining efficiency is low, and slender axles' processing has always been a difficult problem, can lead to work load to increase for guaranteeing the machining precision, and processing is loaded down with trivial details. For multi-cutter synchronous turning, the multi-cutter cutting is mainly applied to the processing of slender shafts, the processing of oil pipes and the drilling in China and abroad mainly aims at the research on the service life of multi-cutters, the processing cost, the quality of processed workpieces, the cutting force and the like. At present, the processing of the slender shaft by adopting multi-cutter synchronous turning is mainly used for processing the polished rod, the flexibility and the universality are lacked, the processing of the cutter synchronism is troublesome, the processing is more complicated, and the dynamic balance performance is not high.
Disclosure of Invention
The utility model provides a synchronous dynamic balance lathe of multitool high efficiency to solve that current traditional lathe work is not enough in machining efficiency that the defect on the mechanism of working leads to, machining precision is not enough, and arouse easily that the processing work piece warp the scheduling problem.
The utility model adopts the technical proposal that: the numerical control lathe comprises a lathe body, a guide rail, a numerical control scale grating, a tailstock, an electric spindle system, a screw I, a workbench driving module and a workbench module; the tailstock is fixed at the tail of the lathe bed, the electric spindle system is fixed at the head of the lathe bed through a first screw, the guide rails are fixed at two sides of the middle of the lathe bed, the numerical control scale grating is fixed at one side of the middle of the lathe bed, the workbench driving module is fixed at the center of the middle of the lathe bed, and the workbench module is fixed on the workbench driving module;
the guide rail comprises a rolling guide rail, a sliding block, a third screw and a fourth screw, the rolling guide rail is fixed on the lathe bed through the fourth screw, and the sliding block is connected with the rolling guide rail in a sliding mode; thereby leading the slide block to slide back and forth on the rolling guide rail and adopting an air-float guide rail;
the workbench driving module comprises a closed end cover, an open end cover, a first bearing seat, a second bearing seat, a workbench screw rod, a workbench connecting piece, a workbench screw rod nut, a third bolt, a coupler, a flange and a first servo motor, wherein the first bearing seat, the second bearing seat and the flange are fixed on the lathe bed, the closed end cover is fixed on the left side of the first bearing seat, the open end cover is fixed on the right side of the second bearing seat, two ends of the workbench screw rod are rotatably connected with corresponding holes of the first bearing seat and the second bearing seat, so that the workbench screw rod can rotate around the axis of the workbench screw rod, the workbench screw rod nut is arranged on the workbench screw rod through a screw rod pair, the workbench connecting piece is fixed on the workbench screw rod nut, the first servo motor is fixed on the flange, the coupler is fixedly connected with the right end of the workbench screw rod and the left end of the first servo motor, so that the workbench screw rod, the workbench connecting piece can move left and right;
the electric spindle system comprises a second screw, an electric spindle base, a first electric spindle bearing end cover, a second electric spindle bearing end cover, a spindle seat, an electric spindle, a second bolt and a three-jaw chuck, wherein the electric spindle base is fixed on the lathe bed through the first screw;
the workbench module comprises a workbench bracket, a first knife rest feeding module, a second knife rest feeding module, a third knife rest feeding module, a gear driving module, a first bolt, a shaft diameter measuring instrument and a grating reading head, wherein the three identical knife rest feeding modules are fixed on the workbench bracket at an angle of 120 degrees, the first knife rest feeding module, the second knife rest feeding module and the third knife rest feeding module are bilaterally symmetrical, and the second knife rest feeding module is positioned in the middle; the gear driving module is fixed at the back of the middle of the workbench bracket, the workbench bracket is fixed on the workbench driving module through a first bolt, and the guide rail supports two sides of the workbench bracket, so that the workbench module can perform axial feeding motion under the driving of the workbench driving module; the shaft diameter measuring instrument is fixed on the workbench bracket, and the grating reading head is fixed on one side of the bottom of the workbench bracket;
the workbench bracket comprises a workbench base, a bolt twelve, a bolt thirteen, a front body bracket, a supporting cover, a rear body bracket, a large gear sleeve, a bolt nine, a bolt ten and a bolt eleven, the workbench base is fixed on the workbench connecting piece of the workbench driving module through a screw I, therefore, the workbench module can be driven by the workbench driving module to axially feed, the front body support is fixed on the workbench base through the thirteen bolts and the twelve bolts, and in order to facilitate the installation of the first tool rest feeding module, the second tool rest feeding module and the third tool rest feeding module, the first tool rest feeding module, the second tool rest feeding module and the third tool rest feeding module are firstly installed on the front body support, and then fixing the support cover on the front body bracket through bolts, thereby realizing the fixation of the first tool rest feeding module, the second tool rest feeding module and the third tool rest feeding module. The rear body support is fixed on the front body support through a bolt nine, the front body support and the rear body support are parallel to each other in the front-back direction, and the large gear sleeve is fixed on the rear body support through a bolt eleven, so that the large bevel gear is rotatably connected on the rear body support, the large bevel gear can rotate around the central axis of the large bevel gear, and the gear driving module drives the tool rest feeding system to perform radial feeding motion;
the gear driving module comprises a small bevel gear, a large bevel gear, a servo motor II, a small straight gear, a supporting seat and a screw eleven, the small bevel gear is meshed with the large bevel gear, the large bevel gear is rotationally connected with a rear body support of the workbench support, the servo motor is fixed on the supporting seat, the small straight gear is fixedly connected with the servo motor, and the supporting plate is fixedly connected with a workbench base of the workbench support through the screw eleven, so that the large bevel gear rotates around the axis of the large bevel gear to drive the tool rest feeding system to perform axial feeding motion under the driving of the servo motor II;
the first tool rest feeding module comprises a feeding mechanism, a switching mechanism and a tool rest, the feeding mechanism is fixedly connected with a front body support of the workbench support, the switching mechanism comprises a fourth bolt, an air cylinder and a first switching connecting piece, the air cylinder is fixedly connected with a rear body support of the workbench support through the fourth bolt, and the first switching connecting piece is fixed on the air cylinder, so that the first switching connecting piece can move radially under the stretching and shrinking of the air cylinder, and the third tool rest feeding module is driven to move radially to switch between a working state and an out-of-operation state;
the tool rest comprises a turning tool base, a turning tool base, a screw nine, a screw five, a motor mounting piece, a screw six, a screw seven, a tool rest connecting piece, a screw eight, a fixing block, a turning tool moving lead screw, a bolt five, a turning tool moving lead screw nut, a taper pin I, a taper pin II and a sleeve, wherein the turning tool base is fixedly connected with the tool rest connecting piece through the screw seven, the tool rest connecting piece is fixed on a feeding mechanism, so that the tool rest can realize radial feeding motion under the driving of the feeding mechanism, the turning tool is fixed on the turning tool base through the screw nine, the turning tool base is in sliding connection with the turning tool base, the turning tool base is fixed on the turning tool moving lead screw nut through the screw five, the motor is fixed on the motor mounting piece through the screw five, the motor mounting piece is fixed on the turning tool, the right end of the lathe tool moving screw rod is fixedly connected with the sleeve through a taper pin I, the sleeve is fixedly connected to the right end of the lathe tool moving screw rod through the taper pin I, and the sleeve is fixedly connected to the left end of the motor through a taper pin II, so that the motor drives the lathe tool moving screw rod to rotate, and the lathe tool moving screw rod further drives the lathe tool to move left and right along the lathe tool base sliding groove through the lathe tool moving screw rod nut;
the feeding mechanism comprises a small bevel gear fixing nut, a first gasket, a first switching connecting piece, a second switching connecting piece, an open bearing end cover, a sixth bolt, a second gasket, a closed bearing end cover, an eighth bolt, a third gasket, a bearing, a seventh bolt, a feeding screw rod nut, a feeding screw rod, a tenth screw and a band-type brake, wherein the small bevel gear fixing nut is fixed at the left end of the feeding screw rod, and a small bevel gear is fixed at the left end of the feeding screw rod nut through the small bevel gear fixing nut and the gasket, so that the feeding screw rod is further driven to rotate by driving the small bevel gear to rotate; the first switching connecting piece is fixedly connected with the feeding screw rod through a spline keyway and movably connected with the second switching connecting piece, so that the first switching connecting piece can drive the feeding mechanism to move radially through the expansion of the cylinder, the second switching connecting piece is fixedly connected with the feeding screw rod through the spline keyway to ensure the tight jacking of the right end of the bevel pinion, the open bearing end cover is fixedly connected with the front bracket of the workbench bracket through a bolt six and a gasket two, the bearing is movably connected with the feeding screw rod, the closed bearing end cover is fixedly connected with the front bracket of the workbench bracket through a bolt eight and a gasket three, the feeding screw rod nut is fixedly connected with the knife rest connecting piece through a bolt seven, the feeding screw rod nut is connected with the feeding screw rod through a screw rod pair, the feeding screw rod is rotatably connected with the front bracket of the workbench bracket, and the rotation of the feeding screw rod is not influenced by the front bracket, the feed screw nut can move left and right along the axial direction of the feed screw under the drive of the feed screw, and further drives the feed mechanism to realize radial movement; the band-type brake is fixedly connected with a front body support of the workbench support through a screw ten, so that the accuracy of radial movement stopping of the feeding mechanism is realized.
The utility model has the advantages that:
1. the traditional turning lathe once can only be used a lathe tool to a curved surface and put at main shaft central point and carry out the turning usually, machining efficiency is low, the utility model discloses the lathe can once be put at main shaft central point and carry out the turning to a curved surface with three or two lathe tools in step, machining efficiency is high.
2. The utility model discloses not only can synchronous processing slender axles when three sword processing methods are selected to the lathe, can also process other gyration type parts such as step shaft and all kinds of complicated curved surfaces in step, also provide new method and thinking for processing slender axles simultaneously.
3. The utility model discloses three lathe tools that the lathe designed are driven by same big bevel gear, have realized three lathe tool feed motion's high synchronization, have reduced the displacement error, have improved the machining precision.
4. The utility model discloses three lathe tools that the lathe designed each interval 120 installation fixed, three lathe tools add the effort that the work piece was treated to the lathe tool and offset each other man-hour, can realize self-supporting and dynamic balance, make and treat that processing work piece atress warp and reduce for the machining precision uprises, and has reduced work load, has saved the time, has improved efficiency, makes the lathe have higher commonality.
5. The utility model discloses three cutters that the lathe designed are mutually independent, and work or the mutual noninterference of out of work can realize 7 different processing methods according to the lathe tool quantity of participating in processing and the position that the lathe tool was located, can adapt to different processing requirements.
6. The utility model discloses the lathe is equivalent to traditional turning lathe under the single-tool mode of processing, can realize the all processing methods of traditional lathe, makes the lathe have higher commonality and practicality.
Drawings
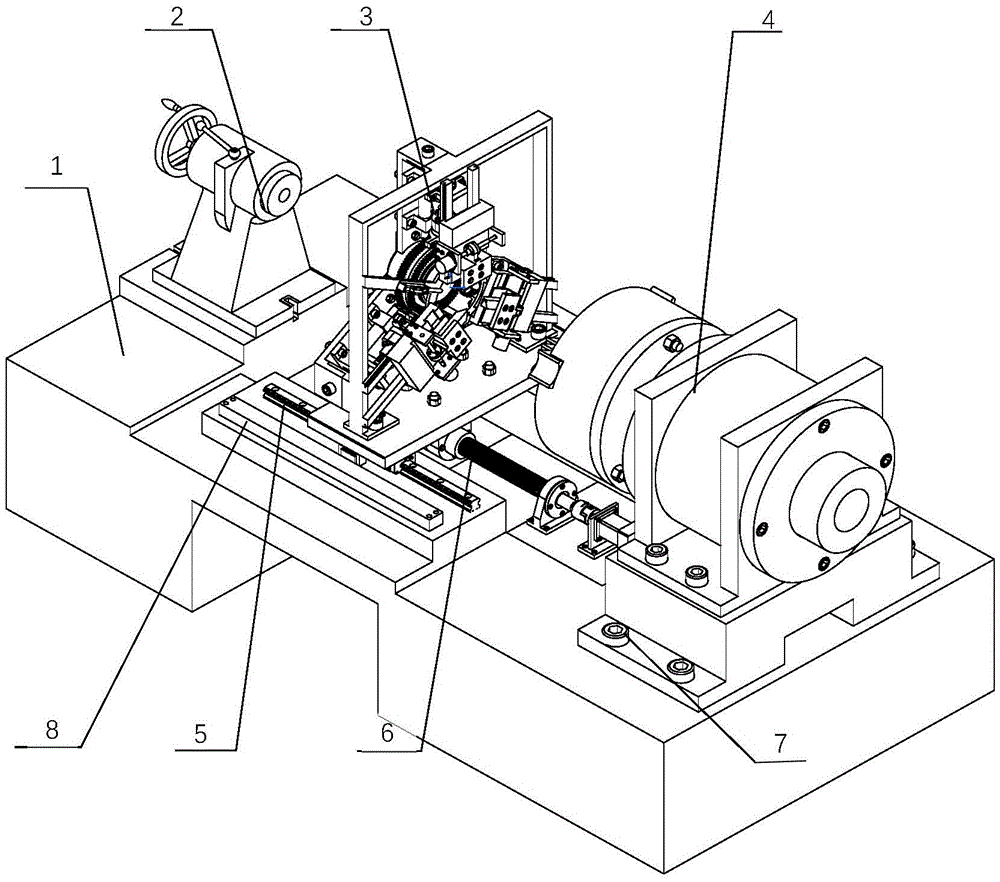
Fig. 1 is a schematic structural diagram of the present invention;
fig. 2 is a schematic structural view of the guide rail of the present invention;
FIG. 3 is a schematic structural diagram of the worktable driving module of the present invention;
fig. 4 is a schematic structural diagram of the electric spindle system of the present invention;
FIG. 5 is a schematic structural diagram of the worktable module of the present invention;
FIG. 6 is a schematic structural view of the worktable bracket of the present invention;
fig. 7 is a schematic mechanism diagram of the gear driving module of the present invention;
fig. 8 is a schematic structural diagram of a first tool rest feeding module according to the present invention;
fig. 9 is a schematic structural diagram of a first tool rest feeding module according to the present invention;
fig. 10 is a schematic structural diagram of a first tool rest feeding module according to the present invention;
fig. 11 is a schematic view of the feed screw of the present invention;
in the figure, a machine tool body 1, a tailstock 2, a workbench module 3, an electric spindle system 4, a guide rail 5, a workbench driving module 6, a screw I7, a numerical control scale grating 8, a tool rest feeding module I301, a workbench support 302, a gear driving module 303, a bolt I304, a tool rest feeding module II 305, a tool rest feeding module III 306, a shaft diameter measuring instrument 307, a grating reading head 308, an electric spindle base 401, an electric spindle 402, an electric spindle bearing end cover I403, a spindle seat 404, an electric spindle bearing end cover II 405, a bolt II 406, a three-jaw chuck 407, a screw II 408, a rolling guide rail 501, a slide block 502, a screw III 503, a screw IV 504, a closed end cover 601, a bearing seat I602, a workbench screw rod 603, a workbench screw rod screw 604, a workbench connecting piece 605, a bolt III 606, a bearing seat II 607, an open end cover 608, a coupling 609, a flange 610, a servo motor I611, a lathe tool base, Lathe tool 30102, lathe tool seat 30103, screw five 30104, motor 30105, motor mounting sheet 30106, screw six 30107, tool rest connecting piece 30108, screw seven 30109, air cylinder 30110, bolt four 30111, switching connecting piece one 30112, screw eight 30113, fixed block 30114, lathe tool moving screw 30115, bolt five 30116, lathe tool moving screw nut 30117, taper pin one 30118, taper pin two 30119, sleeve 30120, screw nine 30121, switching connecting piece two 30122, shim one 30123, bevel pinion fixing nut 30124, open bearing end cover 30125, bolt six 30126, shim two 30127, bearing 30128, bolt seven 30129, feed screw nut 30130, feed screw 30131, screw ten 30132, band brake 30133, closed bearing end cover 30134, bolt eight 30135, shim three 30136, front support 30201, bolt nine 30202, support 30203, rear body bolt 30204, rear body support 30206, large gear 30207, twelve working table base 30209, working table base 3908, and screw eight 30116, Thirteen bolt 30210, a large bevel gear 30301, a small bevel gear 30302, a servo motor 30303, a small spur gear 30304, a support base 30305 and an eleven screw 30306.
Detailed Description
As shown in fig. 1, the numerical control measuring device comprises a lathe bed 1, a guide rail 5, a numerical control scale grating 8, a tailstock 2, an electric spindle system 4, a first screw 7, a workbench driving module 6 and a workbench module 3; the tailstock 2 is fixed at the tail of the lathe body 1, the electric spindle system 4 is fixed at the head of the lathe body 1 through a first screw 7, the guide rails 5 are fixed at two sides of the middle of the lathe body 1, the numerical control scale grating 8 is fixed at one side of the middle of the lathe body 1, the workbench driving module 6 is fixed at the center of the middle of the lathe body 1, and the workbench module 3 is fixed on the workbench driving module 6;
as shown in fig. 2, the guide rail 5 includes a rolling guide rail 501, a sliding block 502, a third screw 503 and a fourth screw 504, the rolling guide rail 501 is fixed on the bed 1 by the fourth screw 504, and the sliding block 502 is connected with the rolling guide rail 501 in a sliding manner; therefore, the sliding block 502 can slide back and forth on the rolling guide rail 501, and an air-floating guide rail is adopted, so that the abrasion is less, and the precision can be kept for a long time;
as shown in fig. 3, the workbench driving module 6 includes a closed end cover 601, an open end cover 608, a first bearing seat 602, a second bearing seat 607, a workbench screw 603, a workbench connecting member 605, a workbench screw nut 604, a third bolt 606, a coupling 609, a flange 610 and a first servo motor 611, wherein the first bearing seat 602, the second bearing seat 607 and the flange 610 are fixed on the machine body 1, the closed end cover 601 is fixed on the left side of the first bearing seat 602, the open end cover 608 is fixed on the right side of the second bearing seat 607, two ends of the workbench screw 603 are rotatably connected with corresponding holes of the first bearing seat 602 and the second bearing seat 607, so that the workbench screw nut 603 can rotate around its own axis, the workbench screw nut 604 is mounted on the workbench screw 603 through a screw pair, the workbench connecting member 605 is fixed on the workbench screw nut 604, the first servo motor 611 is fixed on the flange 610, the coupling 609 fixedly connects the right end of the workbench screw 603 and the, therefore, under the driving of the first servo motor 611, the first workbench lead screw 603 rotates to enable the workbench lead screw nut 604 to accurately feed axially, and the workbench connecting piece 605 can move left and right;
as shown in fig. 4, the electric spindle system 4 includes a second screw 408, an electric spindle base 401, a first electric spindle bearing end cover 403, a second electric spindle bearing end cover 405, a spindle seat 404, an electric spindle 402, a second bolt 406, and a three-jaw chuck 407, where the electric spindle base 401 is fixed to the machine tool body 1 by a first screw 7, the first electric spindle bearing end cover 403 and the second electric spindle bearing end cover 405 are fixed to two ends of the spindle seat 404, the three-jaw chuck 407 is fixed to the end of the electric spindle 402 by a second bolt 406, the spindle seat 404 is fixed to the electric spindle base 401 by a second bolt 408, and the electric spindle 402 is rotationally connected to the spindle seat 404, so that the electric spindle 402 drives a workpiece to be processed to perform a rotational motion by the three-jaw chuck 407 without generating a significant vibration;
as shown in fig. 5, the workbench module 3 includes a workbench bracket 302, a first tool rest feeding module 301, a second tool rest feeding module 305, a third tool rest feeding module 306, a gear driving module 303, a first bolt 304, an axis diameter measuring instrument 307 and a grating reading head 308, wherein the three identical first tool rest feeding modules 301, second tool rest feeding modules 305 and third tool rest feeding modules 306 are fixed on the workbench bracket 302 at an angle of 120 ° with respect to each other, the first tool rest feeding modules 301 and the third tool rest feeding modules 306 are bilaterally symmetrical, and the second tool rest feeding modules 305 are located in the middle; therefore, cutting forces generated on the processed workpiece during turning of the turning tool 30102 can be mutually offset, the deformation of the processed workpiece in the processing process is reduced, and the processing precision is improved; the gear driving module 303 is fixed at the rear of the middle of the workbench bracket 302, the workbench bracket 302 is fixed on the workbench driving module 6 through a first bolt 304, and the guide rail 5 supports two sides of the workbench bracket 302, so that the workbench module 3 can perform axial feeding motion under the driving of the workbench driving module 6; the shaft diameter measuring instrument 307 is fixed on the workbench bracket 302 and used for accurately recording the numerical value of the shaft diameter of the workpiece in turning, and the grating reading head 308 is fixed on one side of the bottom of the workbench bracket 302 and can record and feed back the reading of the numerical control scale grating 8 so as to control the axial feed motion of the workbench module 3;
as shown in fig. 6, the worktable bracket 302 includes a worktable base 30208, a bolt twelve 30209, a bolt thirteen 30210, a forebody bracket 30201, a supporting cover 30203, a rear body bracket 30205, a large gear sleeve 30207, a bolt nine 30202, a bolt ten 30204, and a bolt eleven 30206, the worktable base 30208 is fixed to the worktable connecting member 605 of the worktable driving module 6 by a first bolt 304, so that the worktable module 3 can be axially fed by the worktable driving module 6, the forebody bracket 30201 is fixed to the worktable base 30208 by a bolt thirteen 30210 and a bolt twelve 30209, in order to facilitate the installation of the tool post feed module one 301, the tool post feed module two 305, and the tool post feed module three 306, the tool post feed module one 301, the tool post feed module two 305, and the tool post feed module three 306 are first installed on the forebody bracket 30201, and then the supporting cover 30203 is fixed to the forebody bracket 30201 by a bolt 30204, therefore, the first tool rest feeding module 301, the second tool rest feeding module 305 and the third tool rest feeding module 306 are fixed, the rear body support 30205 is fixed on the front body support 30201 through a bolt nine 30202, the front body support 30201 and the rear body support 30205 are parallel to each other in the front-rear direction, the large gear sleeve 30207 is fixed on the rear body support 30205 through a bolt eleven 30206, and therefore the large bevel gear 30301 is rotatably connected on the rear body support 30205, the large bevel gear 30301 can rotate around the central axis of the large bevel gear 30301, and the gear driving module 303 drives the tool rest feeding system to perform radial feeding movement;
as shown in fig. 7, the gear driving module 303 includes a small bevel gear 30302, a large bevel gear 30301, a servo motor two 30303, a small spur gear 30304, a support base 30305 and a screw eleven 30306, the small bevel gears 30302 are respectively engaged with the large bevel gear 30301, the large bevel gear 30301 is rotatably connected with a rear body support 30205 of the worktable support 302, the servo motor 30303 is fixed to the support base 30305, the small spur gear 30304 is fixedly connected with the servo motor 30303, and the support plate 30305 is fixedly connected with a worktable base 30208 of the worktable support 302 through the screw eleven 30306, so that the large bevel gear 30301 rotates around its axis to drive the tool rest feeding system to perform axial feeding motion under the driving of the servo motor two 30303;
as shown in fig. 8 and 9, the first tool rest feeding module 301 comprises a feeding mechanism, a switching mechanism and a tool rest, the feeding mechanism is fixedly connected with a front body support 30201 of the workbench support 302, the switching mechanism comprises a bolt four 30111, a cylinder 30110 and a switching connecting piece one 30112, the cylinder 30110 is fixedly connected with a rear body support 30205 of the workbench support 302 through the bolt four 30111, and the switching connecting piece one 30112 is fixed on the cylinder 30110, so that the switching connecting piece one 30112 is moved radially under the expansion and contraction of the cylinder 30110, and the tool rest feeding module 301 is driven to move radially to switch between an operating state and an inoperative state;
as shown in fig. 8 and 9, the tool post includes a tool base 30101, a tool 30102, a tool base 30103, a screw set 30121, a screw set 30104, a motor 30105, a motor mounting piece 30106, a screw set 30107, a screw set 30109, a tool post connector 30108, a screw set 30113, a fixing block 30114, a tool moving lead screw 30115, a bolt set 30116, a tool moving lead screw nut 30117, a taper pin set 30118, a taper pin set 30119, and a sleeve 30120, the tool base 30101 is fixedly connected to the tool post connector 30108 through the screw set 30109, the tool post connector 30108 is fixed to the feeding mechanism, so that the tool post can realize radial feeding movement under the driving of the feeding mechanism, the tool 30102 is fixed to the tool base 30103 through the screw set 30121, the tool base 30103 is connected to the tool base 30101 in a sliding manner, the tool base 30103 is fixed to the screw set 30117 through the screw set 30116, the motor 30105 is fixed to the motor mounting piece 30106 through the screw set 30107, the fixed block 30114 is fixed to the lathe tool base 30101 through eight 30113 screws, the left end of the lathe tool moving lead screw 30115 is movably connected to a corresponding hole of the fixed block 30114, the right end of the lathe tool moving lead screw 30120 is fixedly connected to the sleeve 30120 through a taper pin 30118, the sleeve 30120 is fixedly connected to the right end of the lathe tool moving lead screw 30115 through a taper pin 30118, the sleeve 30120 is fixedly connected to the left end of the motor 30105 through a taper pin II 30119, so that the motor 30105 drives the lathe tool moving lead screw 30115 to rotate, the lathe tool moving lead screw 30115 further drives the lathe tool 30102 to move left and right along the chute of the lathe tool;
as shown in fig. 10 and 11, the feeding mechanism includes a bevel pinion fixing nut 30124, a first spacer 30123, a first switching connector 30112, a second switching connector 30122, an open bearing end cover 30125, a sixth bolt 30126, a second spacer 30127, a closed bearing end cover 30134, an eighth bolt 30135, a third spacer 30136, a bearing 30128, a seventh bolt 30129, a feed screw nut 30130, a feed screw 30131, a tenth bolt 30132, and a band-type brake 30133, the bevel pinion fixing nut 30124 is fixed at the left end of the feed screw 30131, and the bevel pinion 30302 is fixed at the left end of the feed screw nut 30130 through the bevel pinion fixing nut 30124 and the spacer 30123, so that the bevel pinion 30302 is driven to rotate to further drive the feed screw 30131; the first switching connecting piece 30112 is fixedly connected with the feed screw 30131 through a spline keyway and movably connected with the second switching connecting piece 30122, so that the first switching connecting piece 30112 drives the feed mechanism to move radially through the expansion and contraction of the air cylinder 30110, the second switching connecting piece 30122 is fixedly connected with the feed screw 30131 through a spline keyway to ensure the tight pushing of the right end of the bevel pinion, the open bearing end cover 30125 is fixedly connected with the front support 30201 of the workbench support 302 through a six bolt 30126 and a two shim 30127, the bearing 30128 is movably connected with the feed screw 30131, the closed bearing end cover 30134 is fixedly connected with the front support 30201 of the workbench support 302 through a eight bolt 30135 and a three shim 30136, the feed screw nut 30130 is fixedly connected with the knife rest connecting piece 30108 through a seven bolt 30129, the feed screw nut 30130 is connected with the feed screw 30131 through a screw pair, the feed screw 30131 is rotatably connected with the front support 30201 of the workbench support 302, thereby realizing that the rotation of the feed screw 30131 is not influenced by the front body support 30201 of the workbench support 302, and the feed screw nut 30130 can move left and right along the axial direction of the feed screw 30131 under the drive of the feed screw 30131, further driving the feed mechanism to realize radial movement; the band-type brake 30133 is fixedly connected with the front support 30201 of the workbench support 302 through a screw 30132, so that the accuracy of radial movement stopping of the feeding mechanism is realized.
The working principle is as follows:
(1) starting a machine tool, determining a machining mode of the machine tool, clamping a blank, measuring a size to be machined related to the blank by using a precision measuring instrument, determining machining allowance, starting machining a workpiece to be machined, and performing finish machining circulation until the precision requirement is met;
(2) when the single-tool machining mode is selected, the single-tool machining modes are three, the most suitable turning tool can be opened among the three turning tools according to the contour of the part and the machining precision requirement, the workpiece to be machined is machined, and different turning tools can be selected for machining according to the requirements during rough machining and finish machining;
(3) when a multi-cutter machining mode is selected, four multi-cutter machining modes are available, three-cutter machining or two-cutter machining can be selected according to the contour of a part and the machining precision requirement, three different modes are selected for the two-cutter machining, in addition, only three-cutter machining or two-cutter machining can be used in rough machining and finish machining, three-cutter machining or two-cutter quick machining can be selected in rough machining, and single-cutter machining can be adopted in finish machining, so that the machining requirements of high efficiency and high precision are met.
According to the processing method of the multi-cutter efficient synchronous dynamic balance turning processing machine tool, when a workpiece is processed, the cylinder 30110 is in an extending state under the default condition, namely the small bevel gear 30302 is meshed with the large bevel gear 30301, the machine tool is in a working mode of simultaneously processing three cutters, and because the three cutters 30102 are installed at intervals of 120 degrees, acting forces of the three cutters 30102 on the workpiece to be processed are mutually offset when the workpiece to be processed is processed, so that the stress deformation of the workpiece to be processed is reduced, and the processing precision is improved; and because the servo motor II 30303 drives the small straight gear 30304 to drive the large bevel gear 30301, and then the large bevel gear further drives the small bevel gear 30302 to rotate at the same time, the three turning tools 30102 can synchronously perform radial feed motion, so that synchronous cutting processing of the workpiece to be processed is realized.
When the machine tool is started for processing, firstly, a motor 30105 is started to adjust the turning tool 30102 to a proper position, and then a servo motor I611 is started to work to move the workbench module 3 to a specific processing area to wait for processing; the electric spindle 402 is started to rotate the workpiece to be processed at a set rotation speed, and the servo motor 30303 is started to enable the turning tool 30102 in a working state to move in the axial direction and the radial direction of the workpiece to be processed. Therefore, the machine tool can realize synchronous linear operation of the first tool rest feeding module 301, the second tool rest feeding module 305 and the third tool rest feeding module 306 along the axial direction of the workpiece to be machined and linear feeding motion along the radial direction of the workpiece to be machined, and additionally realize the rotation motion of the workpiece to be machined, so that the high-efficiency and high-precision machining of a complex curved surface can be realized.
In addition, because the first tool rest feeding module 301, the second tool rest feeding module 305 and the third tool rest feeding module 306 of the tool rest feeding system are mutually independent, the working state of the turning tool 30102 can be switched through the expansion and contraction of the cylinder 30110, when the cylinder 30110 extends out, the turning tool 30102 is in the working state, and when the cylinder 30110 contracts, the turning tool 30102 is in the non-working state, so that there can be 7 processing modes according to the number of the turning tools 30102 participating in processing and the position where the turning tool 30102 is located, wherein the single-tool processing mode is the processing mode of a traditional lathe, so that the turning processing has more flexibility, and the universality and the practicability of the lathe are improved.