CN203509407U - Spot welding tool - Google Patents
Spot welding tool Download PDFInfo
- Publication number
- CN203509407U CN203509407U CN201320401732.2U CN201320401732U CN203509407U CN 203509407 U CN203509407 U CN 203509407U CN 201320401732 U CN201320401732 U CN 201320401732U CN 203509407 U CN203509407 U CN 203509407U
- Authority
- CN
- China
- Prior art keywords
- positioning
- clamping
- workpiece
- clamp body
- spot welding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Landscapes
- Resistance Welding (AREA)
Abstract
本实用新型公开了一种点焊工装,包括手持式焊钳的钳身,在该钳身的钳嘴处设有用于夹持工件的夹持机构,所述夹持机构包括设在所述钳嘴上的两个夹板,其中一个夹板设有定位销,另一个夹板设有与定位销配合的压紧块,压紧块开有让定位销插入的孔。与现有技术相比,本工装采用大力钳的输出力,代替传统夹具的气缸,实现工件的抓取、装配、压紧和松开,适用于小件的夹紧定位,能够确保小件合理定位,工装制作成本低,操作简单。
The utility model discloses a spot welding tool, which comprises a clamp body of a hand-held welding tongs, a clamping mechanism for clamping a workpiece is arranged at the jaw of the clamp body, and the clamping mechanism includes a Two splints on the mouth, one of which is provided with a positioning pin, and the other splint is provided with a pressing block cooperating with the positioning pin, and the pressing block has a hole for the positioning pin to insert. Compared with the existing technology, this tooling adopts the output force of the pliers to replace the cylinder of the traditional fixture to realize the grabbing, assembling, pressing and loosening of the workpiece. It is suitable for the clamping and positioning of small parts and can ensure the reasonableness of small parts Positioning, tooling production costs are low, and the operation is simple.
Description
技术领域 technical field
本实用新型涉及汽车工装,具体地说,本实用新型涉及一种用于汽车白车身焊接的点焊工装。 The utility model relates to automobile tooling, in particular to a spot welding tool used for welding automobile body-in-white. the
背景技术 Background technique
目前,汽车车身上大约90%的焊接都是点焊,每辆车有4000多个焊点。点焊前,对工件进行定位的工装主要是夹具。通过夹具,实现工件快速、准确地定位以及适合的支撑、维持,使生产的所有工件都固定在特定的范围内,保证产品的精密性和互换性。 At present, about 90% of the welding on the car body is spot welding, and each car has more than 4000 welding points. Before spot welding, the tooling for positioning the workpiece is mainly a fixture. Through the fixture, the workpiece can be quickly and accurately positioned and supported and maintained properly, so that all the workpieces produced can be fixed within a specific range, ensuring the precision and interchangeability of the products. the
随着汽车造型的流线型化、车身结构设计的要求越来越高,焊接工艺的难度也越来越大,夹具的投资也是越来越高,厂房面积要求越大越好。针对尺寸较大的冲压件的焊接,夹具定位单位的布置空间充裕,能够保证焊接后的总成件性能和尺寸一致性较好。但对于焊接尺寸较小的零件,往往受这些因素的制约,夹具设计不合理导致焊接一致性差,工艺能力不足。 With the streamlining of automobile modeling and the higher and higher requirements for body structure design, the welding process is becoming more and more difficult, and the investment in fixtures is also getting higher and higher. The larger the workshop area, the better. For the welding of larger stamping parts, the layout space of the fixture positioning unit is sufficient, which can ensure better performance and dimensional consistency of the welded assembly. However, for parts with small welding size, it is often restricted by these factors. Unreasonable fixture design leads to poor welding consistency and insufficient process capability. the
目前的焊接夹具主要存在如下的缺点: The current welding fixture mainly has the following shortcomings:
1、因小件的尺寸限制,难以在夹具上实现充分定位; 1. Due to the size limitation of small parts, it is difficult to achieve sufficient positioning on the fixture;
2、焊接操作比较困难,容易产生质量缺陷(如焊接分流); 2. The welding operation is more difficult and prone to quality defects (such as welding shunt);
3、工位面积不能降低,厂房的利用率不高。 3. The working area cannot be reduced, and the utilization rate of the plant is not high. the
实用新型内容 Utility model content
本实用新型所要解决的技术问题是提供一种点焊工装,以用于汽车白车身的小件在点焊时的定位,确保小件定位合理,方便操作。 The technical problem to be solved by the utility model is to provide a spot welding tool for positioning the small parts of the automobile body-in-white during spot welding, ensuring reasonable positioning of the small parts and convenient operation. the
为了解决上述技术问题,本实用新型所采用的技术方案是:一种点焊工装, 包括手持式焊钳的钳身,在该钳身的钳嘴处设有用于夹持工件的夹持机构;所述夹持机构包括设在所述钳嘴上的两个夹板,其中一个夹板设有定位销,另一个夹板设有与定位销配合的压紧块,压紧块开有让定位销插入的孔。 In order to solve the above-mentioned technical problems, the technical solution adopted in the utility model is: a kind of spot welding tool, comprises the clamp body of hand-held welding tongs, is provided with the clamping mechanism for clamping workpiece at the jaw of this clamp body; The clamping mechanism includes two splints arranged on the mouth of the pliers, one of which is provided with a positioning pin, and the other splint is provided with a pressing block that cooperates with the positioning pin, and the pressing block has a hole for the positioning pin to be inserted into. hole. the
所述定位销和压紧块设有两个。 There are two positioning pins and pressing blocks. the
所述夹板呈U型,所述定位销和压紧块分别设在夹板的两侧。 The splint is U-shaped, and the positioning pins and pressing blocks are respectively arranged on both sides of the splint. the
所述钳身上设有在所述夹持机构夹紧后锁定钳身的锁止机构。 The body of the pliers is provided with a locking mechanism for locking the body of the pliers after clamping by the clamping mechanism. the
本实用新型采用上述技术方案,与现有技术相比,本工装采用大力钳的输出力,代替传统夹具的气缸,实现工件的抓取、装配、压紧和松开,适用于小件的夹紧定位,能够确保小件合理定位,工装制作成本低,操作简单。 The utility model adopts the above-mentioned technical scheme. Compared with the prior art, the utility model adopts the output force of the pliers to replace the cylinder of the traditional fixture to realize the grasping, assembling, pressing and loosening of the workpiece, and is suitable for clamping small pieces. Tight positioning can ensure reasonable positioning of small parts, low cost of tooling production, and simple operation. the
附图说明 Description of drawings
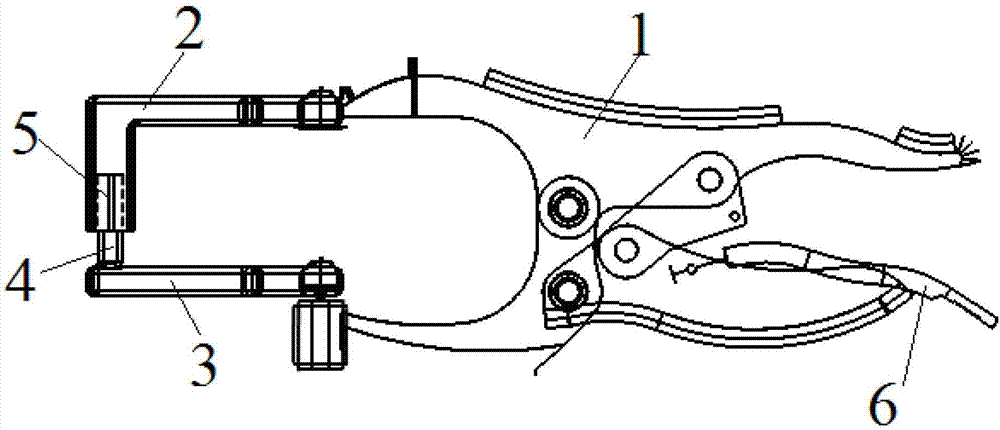
图1为本实用新型的点焊工装的结构示意图; Fig. 1 is the structural representation of spot welding frock of the present utility model;
上述图中的标记均为:1、钳身;2、上夹板;3、下夹板;4、定位销;5、压紧块;6、锁止机构。 The marks in the above figures are: 1. clamp body; 2. upper splint; 3. lower splint; 4. positioning pin; 5. pressing block; 6. locking mechanism. the
具体实施方式 Detailed ways
如图1所示为本实用新型的一种点焊工装,包括手持式焊钳的钳身1,在该钳身1的钳嘴处设有用于夹持工件的夹持机构。在夹持小件时,操作人员手持钳身1,用力握持钳身1的钳臂,钳嘴带动夹持机构压合,实现工件的定位和夹紧。 As shown in FIG. 1 , a spot welding tool of the present invention includes a clamp body 1 of a hand-held welding gun, and a clamping mechanism for clamping a workpiece is provided at the jaw of the clamp body 1 . When clamping a small piece, the operator holds the clamp body 1 and firmly holds the clamp arm of the clamp body 1, and the jaws drive the clamping mechanism to press together to realize the positioning and clamping of the workpiece. the
具体地说,夹持机构包括设在钳嘴上的两个夹板,分别为上夹板2和下夹板3,在下夹板3上设有定位销4,在上夹板2上设有与定位销4配合的压紧块5,压紧块5开有让定位销4插入的孔,工件夹紧在压紧块5和下压板之间,在工件上具有让定位销4穿过的通孔。上夹板2和下夹板3均呈U型,上夹板2和下夹板3在中部与钳身1的钳嘴焊接连接。定位销4和压紧块5均设有两个, 两个定位销4分布在下夹板3的两个伸出部的端部处,压紧块5分布在上夹板2的两个伸出部的端部处。 Specifically, the clamping mechanism includes two splints arranged on the jaws of the pliers, namely the upper splint 2 and the lower splint 3. The lower splint 3 is provided with a positioning pin 4, and the upper splint 2 is provided with a pin that cooperates with the positioning pin 4. The compression block 5 has a hole for positioning pin 4 to insert, and the workpiece is clamped between the compression block 5 and the lower platen, and the workpiece has a through hole for positioning pin 4 to pass through. Both the upper splint 2 and the lower splint 3 are U-shaped, and the upper splint 2 and the lower splint 3 are welded to the jaws of the pliers body 1 in the middle. There are two positioning pins 4 and pressing blocks 5, and the two positioning pins 4 are distributed at the ends of the two extensions of the lower splint 3, and the pressing blocks 5 are distributed at the ends of the two extensions of the upper splint 2. at the end. the
另外,在钳身1上还设有在夹持机构夹紧后锁定钳身1的锁止机构6。钳身1的内部连接有连杆,连杆两端与钳身1的上下手持臂转动铰接,连杆与钳身1的上下手持臂形成四连杆结构。当钳身1在夹紧状态下,内部连杆的凸角撬动锁止机构6,将四连杆结构锁死为三角形结构。若要打开夹持机构,必须压下锁止机构6,才能解锁。 In addition, the clamp body 1 is also provided with a locking mechanism 6 for locking the clamp body 1 after clamping by the clamping mechanism. The inside of the clamp body 1 is connected with a connecting rod, and the two ends of the connecting rod are hinged with the upper and lower holding arms of the clamp body 1, and the connecting rod and the upper and lower holding arms of the clamp body 1 form a four-link structure. When the clamp body 1 is in the clamped state, the protruding corners of the inner connecting rods pry the locking mechanism 6, locking the four-link structure into a triangular structure. To open the clamping mechanism, the locking mechanism 6 must be pressed down to unlock. the
本手持工装具有以下优点: This handheld tool has the following advantages:
1、遵循夹具定位基本“N-2-1”原则,保证工件定位的充分和合理; 1. Follow the basic "N-2-1" principle of fixture positioning to ensure sufficient and reasonable workpiece positioning;
2、实现工件的抓取、装配、压紧、松开功能; 2. Realize the functions of grabbing, assembling, pressing and releasing the workpiece;
3、采用大力钳的输出力,代替传统夹具的气缸,实现制件的夹紧。并有锁紧机构,保证夹紧力的持续恒定; 3. The output force of the vise is used to replace the cylinder of the traditional fixture to realize the clamping of the workpiece. And there is a locking mechanism to ensure the continuous and constant clamping force;
4、该工装的定位部分,可以结合需要焊接的零件形状进行更改,便于大面积的推广; 4. The positioning part of the tooling can be changed in combination with the shape of the parts to be welded, which is convenient for large-scale promotion;
5、本工装配合固定焊钳或者固定点焊机进行焊接即可,减少设备投资,降低操作难度。 5. This tool can be welded with fixed welding tongs or fixed spot welding machine, which reduces equipment investment and operation difficulty. the
上面结合附图对本实用新型进行了示例性描述,显然本实用新型具体实现并不受上述方式的限制,只要采用了本实用新型的方法构思和技术方案进行的各种非实质性的改进,或未经改进将本实用新型的构思和技术方案直接应用于其它场合的,均在本实用新型的保护范围之内。 The utility model has been exemplarily described above in conjunction with the accompanying drawings. Obviously, the specific implementation of the utility model is not limited by the above-mentioned methods, as long as various insubstantial improvements are made by adopting the method concept and technical solutions of the utility model, or Directly applying the ideas and technical solutions of the utility model to other occasions without improvement is within the protection scope of the utility model. the
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320401732.2U CN203509407U (en) | 2013-07-06 | 2013-07-06 | Spot welding tool |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320401732.2U CN203509407U (en) | 2013-07-06 | 2013-07-06 | Spot welding tool |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203509407U true CN203509407U (en) | 2014-04-02 |
Family
ID=50368389
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201320401732.2U Expired - Lifetime CN203509407U (en) | 2013-07-06 | 2013-07-06 | Spot welding tool |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203509407U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN107900589A (en) * | 2017-12-13 | 2018-04-13 | 杭州西奥电梯有限公司 | A kind of welding tooling of moving sidewalk lower part tensioning frame Two bors d's oeuveres |
| CN109540531A (en) * | 2018-12-26 | 2019-03-29 | 绵阳亿丰达智能装备有限公司 | A kind of engine thermal starter clamping and fixing device on probation |
-
2013
- 2013-07-06 CN CN201320401732.2U patent/CN203509407U/en not_active Expired - Lifetime
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN107900589A (en) * | 2017-12-13 | 2018-04-13 | 杭州西奥电梯有限公司 | A kind of welding tooling of moving sidewalk lower part tensioning frame Two bors d's oeuveres |
| CN107900589B (en) * | 2017-12-13 | 2024-03-15 | 杭州西奥电梯有限公司 | Welding fixture for double-splicing of tensioning frame at lower part of automatic sidewalk |
| CN109540531A (en) * | 2018-12-26 | 2019-03-29 | 绵阳亿丰达智能装备有限公司 | A kind of engine thermal starter clamping and fixing device on probation |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN207788109U (en) | Battery tray lifting lug welding tooling | |
| CN107127510B (en) | CMT welding fixture for battery box frame for electric automobile | |
| CN107052665A (en) | A kind of automobile rear-wheel cover seal plate welding assembly welding clamp | |
| CN204997287U (en) | Welding jig of automobile tail -gate planking and tail lamp bedplate | |
| CN101480771B (en) | Projection welding nut welding clamp | |
| CN105665868B (en) | A kind of Contiuum type conducting wire fixture for opposite welding and its manufacturing method | |
| CN201026558Y (en) | Welding clamp used for oil filler hole box of vehicle | |
| CN206185562U (en) | Car shell die casting mills location clamping jig | |
| CN202934305U (en) | Welded clamping tool for circular tube lifting beam of automobile | |
| CN105728890A (en) | Current-carrying sheet welding machine | |
| CN203636249U (en) | Welding fixture for handcart frame in high voltage power distribution cabinet | |
| CN201881091U (en) | Positioning pliers for welding of automobile nuts | |
| CN202336686U (en) | Repair welding clamp | |
| CN203621806U (en) | Compressing wheel stand welding fixture | |
| CN208528385U (en) | A kind of large size adjustable frame structure welding fixture | |
| CN210281179U (en) | Welding positioning tool for automobile oil filler cap | |
| CN214558706U (en) | A clamping and positioning device for flange welding of automobile exhaust system | |
| CN205200885U (en) | Battery installation reinforcing plate fixture device | |
| CN210789776U (en) | Welding gun gripper integrated mechanism | |
| CN205629624U (en) | Current -carrying chip bonding machine | |
| CN202684411U (en) | Auxiliary frame welding fixture | |
| CN202684416U (en) | Auxiliary frame welding fixture | |
| CN205200883U (en) | Back door hinge reinforcing plate fixture device | |
| CN203282098U (en) | Rail-beam two-in-one tool of stentering setting machine | |
| CN205834550U (en) | Power battery base welding fixture |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CX01 | Expiry of patent term | ||
| CX01 | Expiry of patent term |
Granted publication date: 20140402 |