CN202336686U - Repair welding clamp - Google Patents
Repair welding clamp Download PDFInfo
- Publication number
- CN202336686U CN202336686U CN2011205124869U CN201120512486U CN202336686U CN 202336686 U CN202336686 U CN 202336686U CN 2011205124869 U CN2011205124869 U CN 2011205124869U CN 201120512486 U CN201120512486 U CN 201120512486U CN 202336686 U CN202336686 U CN 202336686U
- Authority
- CN
- China
- Prior art keywords
- connecting plate
- groove
- shaft joint
- repair welding
- clamping block
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Butt Welding And Welding Of Specific Article (AREA)
Abstract
本实用新型公开了一种补焊夹具,包括底座,底座上固定有第一连接板,第一连接板的底部与气缸连接,气缸的活塞杆顶端与第一轴接头相连,第一轴接头上铰接有夹紧臂,夹紧臂的中部与第一连接板铰接;底座上与第一连接板相对的一侧固定有第二连接板,第二连接板中设有纵向的滑动装置,滑动装置与第一夹紧块相连;第二连接板靠近气缸的一端开孔,开孔的上方设有与第一轴接头相连的第二轴接头;第二轴接头上铰接有撑杆,撑杆贯穿开孔后固定在第二夹紧块上。本实用新型提供的补焊夹具,装置小巧、结构紧凑,起到了充当补焊工作台的功能,操作简单、省时省力,既增大了焊接强度,减少零部件在焊接中的磨损,又节约了设备成本,提高工作效率。
The utility model discloses a repair welding fixture, which comprises a base, on which a first connecting plate is fixed, the bottom of the first connecting plate is connected with the cylinder, the top end of the piston rod of the cylinder is connected with the first shaft joint, and the first shaft joint is A clamping arm is hinged, and the middle part of the clamping arm is hinged with the first connecting plate; a second connecting plate is fixed on the side opposite to the first connecting plate on the base, and a longitudinal sliding device is arranged in the second connecting plate. It is connected with the first clamping block; a hole is opened at the end of the second connecting plate close to the cylinder, and a second shaft joint connected with the first shaft joint is arranged above the opening; a strut is hinged on the second shaft joint, and the strut runs through After opening the hole, it is fixed on the second clamping block. The repair welding jig provided by the utility model has a small device and a compact structure, and functions as a repair welding workbench. Reduce equipment costs and improve work efficiency.
Description
技术领域 technical field
本实用新型涉及一种汽车制造中的夹具,具体涉及一种用于汽车焊装生产线上的补焊夹具。 The utility model relates to a jig in automobile manufacturing, in particular to a repair welding jig used in an automobile welding production line. the
背景技术 Background technique
目前汽车焊装生产线上焊接零部件时,通常需要用焊接夹具夹紧定位,现有的焊装夹具,主要包括底座、固定在底座上的连接板、与连接板相连的气缸、与气缸的活塞杆铰接的夹紧臂等结构。众所周知,不同形状尺寸的零部件,所用的焊接夹具也各有千秋。对于形状复杂、焊接要求高的零部件,对焊接夹具的要求也较高、结构也较复杂,因此使用复杂的焊接夹具时,夹具的夹紧块可能会遮挡住部分焊接位置而无法进行点焊。 At present, when welding parts on the automobile welding production line, welding fixtures are usually used for clamping and positioning. The existing welding fixtures mainly include a base, a connecting plate fixed on the base, a cylinder connected to the connecting plate, and a piston connected to the cylinder. Structures such as clamping arms with hinged rods. As we all know, the welding fixtures used for parts of different shapes and sizes also have their own advantages and disadvantages. For parts with complex shapes and high welding requirements, the requirements for welding fixtures are also high and the structure is more complicated. Therefore, when using complex welding fixtures, the clamping block of the fixture may cover part of the welding position and spot welding cannot be performed. . the
针对前述的复杂的焊接夹具无法全方位点焊的缺陷,多数厂家通过采用增设多个工位来完成全部的焊接。具体而言,即先夹紧零件焊接部分定位焊点,然后松开夹具将零部件取出放置于夹紧臂上充当补焊工作台,或将零部件转移至其他工位上进行补焊。上述技术方案的不足之处在于:①若直接将零部件放在夹紧臂上未固定补焊,易磨损零部件的定位精度,从而影响车身精度;同时,这种补焊方式易使零部件在补焊中滑动碰撞,影响焊接强度;②若将零部件转移至其他工位上进行补焊,这种焊钳分流、增设工位的方式,将增大设备成本,造成资源浪费,也降低了工作效率。 In view of the above-mentioned defect that the complex welding fixtures cannot be spot-welded in all directions, most manufacturers complete all the welding by adding multiple stations. Specifically, the welding part of the part is first clamped to position the welding spot, and then the clamp is released to take out the part and place it on the clamping arm as a repair welding workbench, or transfer the part to another station for repair welding. The disadvantages of the above technical solutions are: ①If the parts are directly placed on the clamping arm without fixing the repair welding, the positioning accuracy of the easily worn parts will affect the accuracy of the vehicle body; at the same time, this repair welding method will easily make the parts Sliding and collision during repair welding will affect the welding strength; ② If the parts are transferred to other stations for repair welding, this method of diverting welding tongs and adding stations will increase equipment costs, cause waste of resources, and reduce work efficiency. the
实用新型内容 Utility model content
本实用新型提供了一种补焊夹具,解决了采用现有焊接夹具将造成零部件易磨损、焊接强度差、设备成本高、工作效率低的技术缺陷。 The utility model provides a repair welding jig, which solves the technical defects of easy wear of parts, poor welding strength, high equipment cost and low work efficiency caused by the existing welding jig. the
本实用新型所采用的技术方案具体如下: The technical scheme adopted in the utility model is specifically as follows:
一种补焊夹具,包括底座,底座上固定有第一连接板,第一连接板的底部与气缸连接,气缸的活塞杆顶端与第一轴接头相连,第一轴接头上铰接有夹紧臂,夹紧臂的中部与第一连接板铰接;底座上、与第一连接板相 对的一侧固定有第二连接板,第二连接板中设有纵向的滑动装置,滑动装置与第一夹紧块相连;第二连接板靠近气缸的一端开孔,开孔的上方设有与第一轴接头相连的第二轴接头;第二轴接头上铰接有撑杆,撑杆贯穿开孔后固定在第二夹紧块上。 A repair welding fixture, comprising a base, on which a first connecting plate is fixed, the bottom of the first connecting plate is connected to a cylinder, the top end of a piston rod of the cylinder is connected to a first shaft joint, and a clamping arm is hinged on the first shaft joint , the middle part of the clamping arm is hinged with the first connecting plate; on the base, a second connecting plate is fixed on the side opposite to the first connecting plate, and a longitudinal sliding device is arranged in the second connecting plate, which is connected with the first connecting plate The clamping blocks are connected; a hole is opened at the end of the second connecting plate close to the cylinder, and a second shaft joint connected with the first shaft joint is arranged above the opening; a strut is hinged on the second shaft joint, and the strut passes through the hole Fixed on the second clamping block. the
在优选的技术方案中,滑动装置包括纵向的滑槽和在滑槽内上下滑动的滑杆,滑槽内外贯通第二连接板,滑杆与第一夹紧块固定相连。 In a preferred technical solution, the sliding device includes a longitudinal chute and a sliding bar sliding up and down in the chute, the chute passes through the second connecting plate inside and outside, and the sliding bar is fixedly connected with the first clamping block. the
在更优选的技术方案中,第一夹紧块通过螺栓与滑杆固定相连;使得第一夹紧块在滑槽内上下滑动,即可手动调整第一夹紧块与第二夹紧块之间的间距,便于夹持零部件,进行补焊。 In a more preferred technical solution, the first clamping block is fixedly connected to the slide bar through bolts; the first clamping block slides up and down in the chute, and the distance between the first clamping block and the second clamping block can be manually adjusted. The distance between them is convenient for clamping parts and repairing welding. the
在优选的技术方案中,第一轴接头为凹槽结构,凹槽的凹口向上,凹槽的底部与气缸的活塞杆相连,凹槽的两壁设有与夹紧臂铰接的第一连接杆。 In the preferred technical solution, the first shaft joint is a groove structure, the notch of the groove is upward, the bottom of the groove is connected with the piston rod of the cylinder, and the two walls of the groove are provided with the first connection hinged with the clamping arm pole. the
在优选的技术方案中,第二轴接头为凹槽结构,凹槽的凹口向外,凹槽的底部与第一连接杆相连,凹槽的两壁设有与撑杆铰接的第二连接杆。上述第一轴接头、第二轴接头的技术方案设计,使得当气缸通气产生作用力后,夹紧臂、撑杆、与撑杆固定相连的第二夹紧块均能相应受力而运动。 In the preferred technical solution, the second shaft joint is a groove structure, the notch of the groove is outward, the bottom of the groove is connected with the first connecting rod, and the two walls of the groove are provided with a second connection hinged with the support rod pole. The above-mentioned technical design of the first shaft joint and the second shaft joint enables the clamping arm, the strut, and the second clamping block fixedly connected to the strut to move under force when the cylinder is ventilated to generate force. the
在优选的技术方案中,第一连接板的上部开槽,夹紧臂的前部设有与第一连接板相配合的开槽。 In a preferred technical solution, the upper part of the first connecting plate is slotted, and the front part of the clamping arm is provided with a slot matching the first connecting plate. the
在更优选的技术方案中,第一连接板的上部设有开口向上的凹槽,夹紧臂的前部设有开口向下的凹槽;凹槽主要是为了能够更平稳的安放不同形状的零部件。 In a more preferred technical solution, the upper part of the first connecting plate is provided with a groove with an upward opening, and the front part of the clamping arm is provided with a groove with a downward opening; the groove is mainly for more stable placement of different shapes parts. the
在优选的技术方案中,第一夹紧块与第二夹紧块上下平行。 In a preferred technical solution, the first clamping block is vertically parallel to the second clamping block. the
本实用新型提供的补焊夹具,装置小巧、结构紧凑,夹具各部件之间多采用活动连接,便于拆卸维修和精度调节;同时,在现有的焊接夹具基础上改造,增设了第一夹紧块、第二夹紧块等夹紧机构,起到了充当补焊工作台的功能,操作简单、省时省力,既增大了焊接强度,减少零部件在焊接中的磨损,又节约了设备成本,提高工作效率。本实用新型提供的补焊夹具,还可将多个夹具联合使用,共同夹持较复杂的零部件,通用性强,能适用于需要补焊的各种工位。 The repair welding jig provided by the utility model has a small device and a compact structure, and the parts of the jig are mostly connected with each other, which is convenient for disassembly and maintenance and precision adjustment; at the same time, the first clamping is added on the basis of the existing welding jig. Clamping mechanisms such as the first clamping block and the second clamping block function as repair welding workbenches. The operation is simple, time-saving and labor-saving, which not only increases the welding strength, reduces the wear of parts during welding, but also saves equipment costs. ,Improve work efficiency. The repair welding fixture provided by the utility model can also be used in conjunction with multiple fixtures to jointly clamp more complicated parts, has strong versatility, and can be applied to various stations that need repair welding. the
附图说明 Description of drawings
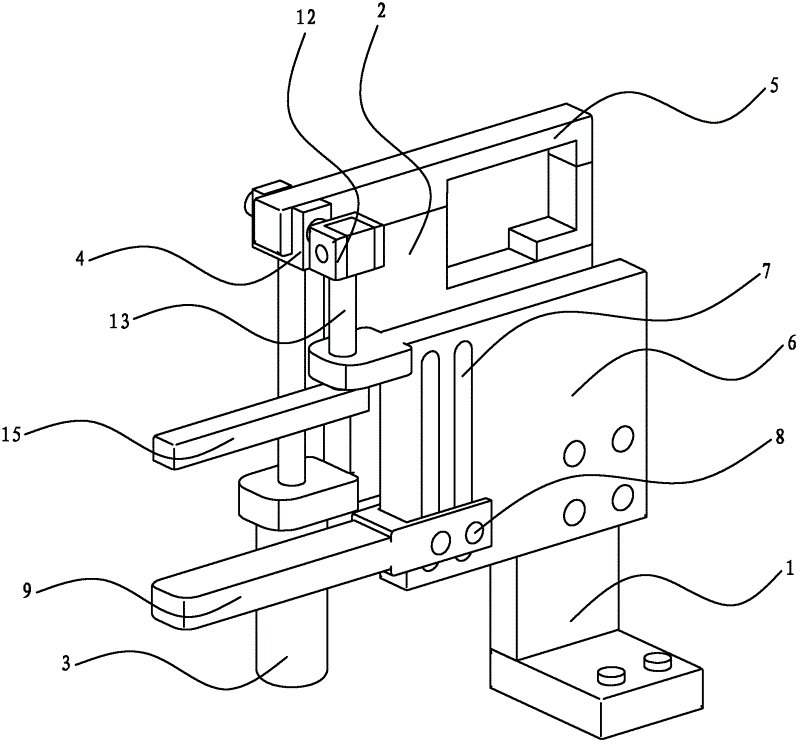
图1为本实用新型补焊夹具的立体结构示意图。 Fig. 1 is a three-dimensional structural schematic diagram of the repair welding fixture of the present invention. the
图2为本实用新型补焊夹具的正面结构示意图。 Fig. 2 is a schematic view of the front structure of the repair welding jig of the present invention. the
图3为本实用新型补焊夹具的侧视结构示意图。 Fig. 3 is a side view structural schematic diagram of the repair welding fixture of the present invention. the
图4为多个本实用新型补焊夹具装配在一起的工作示意图。 Fig. 4 is a working schematic diagram of a plurality of welding repair fixtures of the present invention assembled together. the
具体实施方式 Detailed ways
如图1和图2所示,一种补焊夹具,包括底座1,底座1为L形结构,底座1上部的一侧固定有第一连接板2,第一连接板2的底部与气缸3连接,气缸3的活塞杆顶端与第一轴接头4相连,第一轴接头4与夹紧臂5的一端铰接,夹紧臂5的中部与第一连接板2的上部铰接。
As shown in Figures 1 and 2, a repair welding fixture includes a
底座1上部的另一侧固定有第二连接板6,第二连接板6的位置与第一连接板2相对;第二连接板6中设有纵向的滑动装置,滑动装置包括纵向的滑槽7和可在滑槽7内上下滑动的滑杆8,滑槽7内外贯通第二连接板6,滑杆8上套有第一夹紧块9,并在滑杆8的两端用螺栓将第一夹紧块9拧紧固定。
The other side of the upper part of the
本实用新型中的滑动装置,不限于本实施例中提及的滑槽7和滑杆8这种结构形式,只要满足与滑动装置相连的第一夹紧块9能够进行上下滑动的即可。同时,也不限于滑杆8套螺栓这种固定方式,只要满足第一夹紧块9固定在滑动装置上的即可。
The sliding device in the present invention is not limited to the structural form of the
此外,第一连接板2的上部设有开口向上的凹槽,夹紧臂5的前部设有开口向下、且与第一连接板2的凹槽位置配对的凹槽。
In addition, the upper part of the first connecting
如图3所示,第一轴接头4为凹槽结构,凹槽的凹口向上,凹槽的底部与气缸3的活塞杆相连,凹槽的两壁设有与夹紧臂5铰接的第一连接杆10。
As shown in Figure 3, the
第二连接板6的上部、靠近气缸3的一端设有开孔11,开孔11的上方设有与第一轴接头4相连的第二轴接头12;第二轴接头12也为凹槽结构,凹槽的凹口向外,凹槽的底部与第一连接杆10相连,凹槽的两壁设有与撑杆13铰接的第二连接杆14。
The upper part of the second connecting plate 6, one end close to the
如前所述,撑杆13的一端与第二轴接头12铰接,撑杆13的另一端贯穿开孔11后固定在第二夹紧块15上。
As mentioned above, one end of the
本实用新型提供的补焊夹具,工作过程具体如下: The working process of the repair welding fixture provided by the utility model is as follows:
将本实用新型补焊夹具放置于工作台上,通过螺栓将夹具的底座1固定在工作台上;取待焊接的零部件,放在第一连接板2上部的凹槽中,启动气缸3。
Place the repair welding fixture of the present utility model on the workbench, fix the
气缸3通气后,其活塞杆带动夹紧臂5下降,夹持住零部件后,对部分焊接位进行点焊。
After the
点焊完成后,启动气缸3,使得夹紧臂5上升,取出零部件,翻转侧放于第一夹紧块9和第二夹紧块15之间;根据零部件的实际大小,可上下滑动第一夹紧块9调整间距,以便于夹持住零部件。
After the spot welding is completed, start the
调整完成后,再次启动气缸3,其活塞杆依次带动第一轴接头4、第二轴接头12、撑杆13,使得与撑杆13固定相连的第二夹紧块15下降,牢固夹持住零部件,对之前未焊接到的位置进行补焊。
After the adjustment is completed, start the
补焊完成后,操作同上,启动气缸3,取出已焊接好的零部件。
After the repair welding is completed, the operation is the same as above, start the
若要焊接较复杂的大型零部件,可将多个本实用新型的补焊夹具装置一起装配在工作台上,装配位置如图4所示,左右、前后对称地装配四个补焊夹具,左右两个补焊夹具的中间装配第一支座16,工作台的前端再装配第二支座17;将零部件架在夹紧臂5与第一连接板2的凹槽中,进行初焊,初焊完成后,操作同前述的使用过程,将零部件翻转侧放于第一夹紧块9和第二夹紧块15之间,进行补焊。
If you want to weld more complex large-scale parts, you can assemble a plurality of repair welding fixture devices of the present utility model together on the workbench. The assembly position is shown in Figure 4. The
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011205124869U CN202336686U (en) | 2011-12-09 | 2011-12-09 | Repair welding clamp |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011205124869U CN202336686U (en) | 2011-12-09 | 2011-12-09 | Repair welding clamp |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202336686U true CN202336686U (en) | 2012-07-18 |
Family
ID=46485390
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2011205124869U Expired - Fee Related CN202336686U (en) | 2011-12-09 | 2011-12-09 | Repair welding clamp |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202336686U (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102862016A (en) * | 2012-10-19 | 2013-01-09 | 江苏腾旋科技股份有限公司 | Adjustable welding mechanism for tail cover |
| CN103495831A (en) * | 2013-10-18 | 2014-01-08 | 宁波泰立电子科技有限公司 | Port resonator high-frequency welding fixture |
| CN103862482A (en) * | 2013-11-14 | 2014-06-18 | 浙江吉利控股集团有限公司 | Positioning fixture for repairing welding of workpiece gripped by robot |
-
2011
- 2011-12-09 CN CN2011205124869U patent/CN202336686U/en not_active Expired - Fee Related
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102862016A (en) * | 2012-10-19 | 2013-01-09 | 江苏腾旋科技股份有限公司 | Adjustable welding mechanism for tail cover |
| CN102862016B (en) * | 2012-10-19 | 2014-09-03 | 江苏腾旋科技股份有限公司 | Adjustable welding mechanism for tail cover |
| CN103495831A (en) * | 2013-10-18 | 2014-01-08 | 宁波泰立电子科技有限公司 | Port resonator high-frequency welding fixture |
| CN103495831B (en) * | 2013-10-18 | 2015-04-15 | 宁波泰立电子科技有限公司 | Port resonator high-frequency welding fixture |
| CN103862482A (en) * | 2013-11-14 | 2014-06-18 | 浙江吉利控股集团有限公司 | Positioning fixture for repairing welding of workpiece gripped by robot |
| CN103862482B (en) * | 2013-11-14 | 2016-01-20 | 浙江吉利控股集团有限公司 | A kind of robot grip repair welding positioning tool |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103317236B (en) | Lithium battery laser welding machine | |
| CN105014371B (en) | Rod Automatic Drilling Machine | |
| CN203696271U (en) | Flexible welding tool for forklift gantries | |
| CN205551860U (en) | Crashproof roof beam welding jig before car | |
| CN205325143U (en) | Car seat slide rail assembly machine | |
| CN103862482A (en) | Positioning fixture for repairing welding of workpiece gripped by robot | |
| CN201792225U (en) | Fixture integrated with functions of positioning and bore spot welding | |
| CN205834839U (en) | A kind of processing jig of mobile phone gadget inner chamber | |
| CN205147631U (en) | Robot is welding bench in turn | |
| CN202591897U (en) | Impulse welding axle housing positioning and welding half-axle system | |
| CN102554537B (en) | Positioning and clamping mechanism of welding fixture of automobile stamping piece | |
| CN206185562U (en) | Car shell die casting mills location clamping jig | |
| CN208234119U (en) | A kind of automatical and efficient ladder fixture | |
| CN103753247A (en) | Double-arm single-action hinge clamping device | |
| CN106112356B (en) | A kind of grillage welding bench | |
| CN206216326U (en) | A kind of pneumatic efficient rotary work piece special fixture | |
| CN203621806U (en) | Compressing wheel stand welding fixture | |
| CN206588516U (en) | For electrolytic cell cathode steel bar and the welding tool setup of explosion block | |
| CN207840551U (en) | A kind of automobile component positioning welding pre- clamping centering clamping pneumatic structure manually | |
| CN202684411U (en) | Auxiliary frame welding fixture | |
| CN105436801A (en) | Welded reducer gearbox body assembling quick positioning tool | |
| CN205708816U (en) | The transposition unit of travel switch contact part kludge | |
| CN204603640U (en) | Air-spring type full loading carriage back segment skeleton welding fixture special | |
| CN202684416U (en) | Auxiliary frame welding fixture | |
| CN203245547U (en) | A laser welding jig |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20120718 Termination date: 20131209 |