CN202607158U - Adjustable welding jig for safety belt reinforced plate - Google Patents
Adjustable welding jig for safety belt reinforced plate Download PDFInfo
- Publication number
- CN202607158U CN202607158U CN2012202379837U CN201220237983U CN202607158U CN 202607158 U CN202607158 U CN 202607158U CN 2012202379837 U CN2012202379837 U CN 2012202379837U CN 201220237983 U CN201220237983 U CN 201220237983U CN 202607158 U CN202607158 U CN 202607158U
- Authority
- CN
- China
- Prior art keywords
- guide rail
- electrode column
- welded
- safety belt
- positioning
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Landscapes
- Butt Welding And Welding Of Specific Article (AREA)
Abstract
本实用新型公开了一种可调式安全带加强板焊接夹具,包括有支架,所述支架上架设有导轨,所述导轨上滑动配合有两定位座,所述两定位座之间的导轨上还滑动配合有电极柱定位块,所述电极柱定位块的左、右侧面分别为弧形凹槽,所述弧形凹槽与电极柱配合,所述导轨上方设有气缸驱动的压板,所述压板上设有滑槽,所述滑槽上配合安装有可移动的压块和工件定位块,所述定位座、电极柱定位块、压块以及工件定位块上分别设有锁紧孔,且分别通过锁紧螺栓锁紧在导轨和压板上。本实用新型结构设计合理,为安全带加强板焊接时的专用夹具,操作方便实用且维护方便,成本低廉,提高了工作效率,可满足不同型号、不同尺寸的安全带加强板焊接的需要,实现了一机多用。
The utility model discloses an adjustable safety belt reinforcing plate welding fixture, which includes a bracket, a guide rail is erected on the bracket, and two positioning seats are slidably fitted on the guide rail, and there are also two positioning seats on the guide rail between the two positioning seats. The electrode column positioning block is slidably matched. The left and right sides of the electrode column positioning block are respectively arc-shaped grooves, and the arc-shaped groove is matched with the electrode column. The pressure plate is provided with a chute, and the chute is equipped with a movable pressing block and a workpiece positioning block. The positioning seat, the electrode column positioning block, the pressing block and the workpiece positioning block are respectively provided with locking holes. And they are respectively locked on the guide rail and the pressing plate by locking bolts. The utility model has a reasonable structural design and is a special fixture for seat belt reinforcement plate welding. It is convenient and practical to operate, easy to maintain, low in cost, and improves work efficiency. It can meet the needs of different types and sizes of seat belt reinforcement plate welding One machine with multiple functions.
Description
技术领域 technical field
本实用新型主要涉及一种焊接夹具,尤其涉及一种可调式安全带加强板焊接夹具。 The utility model mainly relates to a welding jig, in particular to an adjustable safety belt reinforcing plate welding jig.
背景技术 Background technique
一般安全带加强板需要点凸焊,要求两个钣金件(螺母安装板和安全带加强板)边缘平行,而只有两个焊点,如果在机器人焊接成本过高且浪费时间,或悬点焊机上焊接因其体积较小,焊接设备活动区域非常小,手动操作不便,效率不高,不能满足批量加工成产的要求。 Generally, seat belt reinforcement boards require spot welding, which requires that the edges of the two sheet metal parts (nut mounting plate and seat belt reinforcement board) be parallel, and there are only two welding spots. Welding on the welding machine is small in size, the active area of the welding equipment is very small, manual operation is inconvenient, and the efficiency is not high, which cannot meet the requirements of batch processing and production.
实用新型内容 Utility model content
本实用新型的目的是为了弥补已有技术的不足,提供了一种安全带加强板焊接专用夹具,解决了采用机器人焊接成本过高且浪费时间,或悬点焊机上焊接因其体积较小,焊接设备活动区域非常小,手动操作不便,效率不高等问题。 The purpose of the utility model is to make up for the deficiencies of the prior art, and to provide a special fixture for seat belt reinforcement plate welding, which solves the high cost and time-wasting of robot welding, or the small size of the welding on the suspension spot welder. , The active area of welding equipment is very small, manual operation is inconvenient, and the efficiency is not high.
本实用新型是通过以下技术方案来实现的: The utility model is achieved through the following technical solutions:
一种可调式安全带加强板焊接夹具,包括有支架,所述支架上架设有导轨,所述导轨上滑动配合有两定位座,所述两定位座之间的导轨上还滑动配合有电极柱定位块,所述电极柱定位块的左、右侧面分别为弧形凹槽,所述弧形凹槽与电极柱配合,所述导轨上方设有气缸驱动的上、下压板,所述下压板上设有滑槽,所述滑槽上配合安装有可移动的压块和工件定位块,所述定位座、电极柱定位块、压块以及工件定位块上分别设有锁紧孔,且分别通过锁紧螺栓锁紧在导轨和压板上。 An adjustable safety belt reinforcement plate welding fixture, including a bracket, a guide rail is set on the bracket, and two positioning seats are slidably fitted on the guide rail, and an electrode column is also slidably fitted on the guide rail between the two positioning seats Positioning block, the left and right sides of the electrode column positioning block are respectively arc-shaped grooves, the arc-shaped grooves are matched with the electrode column, and the upper and lower pressure plates driven by the cylinder are arranged above the guide rail. The pressing plate is provided with a chute, and the chute is equipped with a movable pressing block and a workpiece positioning block. The positioning seat, the electrode column positioning block, the pressing block and the workpiece positioning block are respectively provided with locking holes, and They are respectively locked on the guide rail and the pressure plate by locking bolts.
所述的定位座与待焊接安全带加强板的两侧配合,所述工件定位块与与待焊接安全带加强板的上端面向贴合,同时与待焊接螺母安装板的侧面贴合,压块的下端面与待焊接螺母安装板上端面贴合,且将待焊接螺母安装板和待焊接安全带加强板固定的相对稳定。 The positioning seat cooperates with both sides of the safety belt reinforcement plate to be welded, and the workpiece positioning block fits with the upper surface of the safety belt reinforcement plate to be welded, and at the same time fits with the side of the nut mounting plate to be welded. The lower end surface of the lower end surface is attached to the end surface of the nut mounting plate to be welded, and the nut mounting plate to be welded and the safety belt reinforcement plate to be welded are fixed relatively stably.
其原理是:通过两定位座和工件定位块将螺母安装板定位住而不会旋转,同时安全带加强板放置到螺母安装板上通过压块固定,同时配合工件定位块与与待焊接螺母安装板的侧面贴合,同样也不会旋转,且边缘与螺母安装板平行,由气缸带动压板运动压住螺母安装板、安全带加强板使之贴合紧密;通过电极定位块两边设有弧形凹槽,将电极柱卡在弧形凹槽中以保障焊点的位置,采用此夹具灵活操作方便实用且维护方便,成本低廉;同时定位座、压块和工件定位块的位置可调,可满足不同型号、不同尺寸的安全带加强板焊接的需要,实现了一机多用。 The principle is: through the two positioning seats and the workpiece positioning block, the nut mounting plate is positioned without rotation, and at the same time, the safety belt reinforcement plate is placed on the nut mounting plate and fixed by the pressure block, and at the same time, it is installed with the workpiece positioning block and the nut to be welded. The side of the plate fits together, and it will not rotate, and the edge is parallel to the nut mounting plate. The cylinder drives the pressure plate to press the nut mounting plate and the seat belt reinforcement plate to make them fit tightly; the two sides of the electrode positioning block are provided with arcs Groove, the electrode column is clamped in the arc-shaped groove to ensure the position of the solder joint. Using this fixture is flexible, convenient, practical, easy to maintain, and low in cost; at the same time, the positions of the positioning seat, the pressing block and the workpiece positioning block are adjustable. It meets the welding needs of seat belt reinforcement plates of different models and sizes, and realizes one machine with multiple functions.
本实用新型的优点是: The utility model has the advantages of:
本实用新型结构设计合理,为安全带加强板焊接时的专用夹具,操作方便实用且维护方便,成本低廉,提高了工作效率,可满足不同型号、不同尺寸的安全带加强板焊接的需要,实现了一机多用。 The utility model has a reasonable structural design and is a special fixture for seat belt reinforcement plate welding. It is convenient and practical to operate, easy to maintain, low in cost, and improves work efficiency. It can meet the needs of different types and sizes of seat belt reinforcement plate welding One machine with multiple functions.
附图说明 Description of drawings
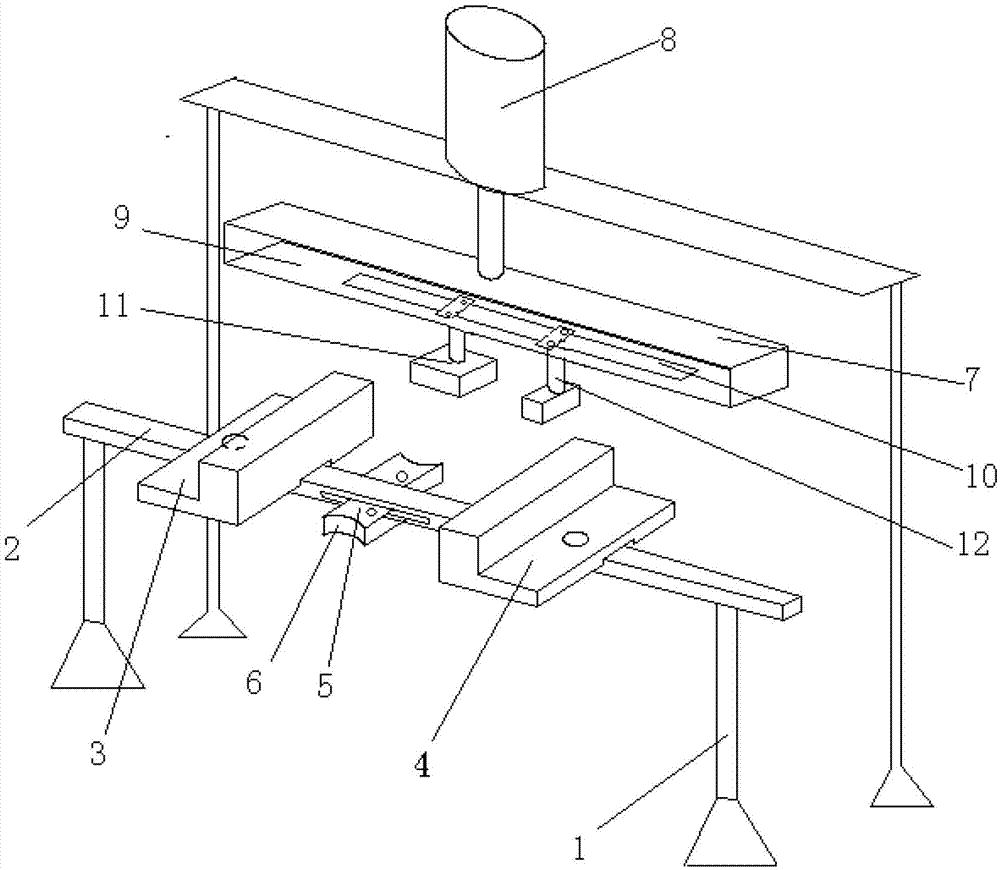
图1 为本实用新型结构示意图。 Fig. 1 is the structural representation of the utility model.
具体实施方式 Detailed ways
参见附图,一种可调式安全带加强板焊接夹具,包括有支架1,支架1上架设有导轨2,导轨2上滑动配合有两定位座3、4,两定位座3、4之间的导轨2上还滑动配合有电极柱定位块5,电极柱定位块5的左、右侧面分别为弧形凹槽6,弧形凹槽6与电极柱配合,导轨2上方设有气缸8驱动的上、下压板7、9,下压板9上设有滑槽10,滑槽10上配合安装有可移动的压块11和工件定位块12,定位座3、4、电极柱定位块5、压块11以及工件定位块12上分别设有锁紧孔,且分别通过锁紧螺栓锁紧在导轨2和压板上;所述的定位座3、4与待焊接安全带加强板的两侧配合,工件定位块12与与待焊接安全带加强板的上端面向贴合,同时与待焊接螺母安装板的侧面贴合,压块11的下端面与待焊接螺母安装板上端面贴合,且将待焊接螺母安装板和待焊接安全带加强板固定的相对稳定。 Referring to the accompanying drawings, an adjustable safety belt reinforcement plate welding fixture includes a bracket 1, a guide rail 2 is mounted on the bracket 1, and two positioning seats 3, 4 are slidably fitted on the guide rail 2, and the gap between the two positioning seats 3, 4 The guide rail 2 is also slidably fitted with an electrode column positioning block 5. The left and right sides of the electrode column positioning block 5 are respectively arc-shaped grooves 6. The arc-shaped groove 6 is matched with the electrode column. The upper and lower pressing plates 7,9, the lower pressing plate 9 is provided with a chute 10, the chute 10 is equipped with a movable pressing block 11 and a workpiece positioning block 12, positioning seats 3,4, electrode column positioning block 5, The pressure block 11 and the workpiece positioning block 12 are respectively provided with locking holes, and are respectively locked on the guide rail 2 and the pressure plate by locking bolts; the positioning seats 3, 4 are matched with the two sides of the safety belt reinforcement plate to be welded , the workpiece positioning block 12 is attached to the upper surface of the seat belt reinforcement plate to be welded, and is attached to the side surface of the nut mounting plate to be welded, and the lower end surface of the pressure block 11 is attached to the upper surface of the nut mounting plate to be welded, and the The nut mounting plate to be welded and the safety belt reinforcing plate to be welded are fixed relatively stably.
Claims (2)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012202379837U CN202607158U (en) | 2012-05-24 | 2012-05-24 | Adjustable welding jig for safety belt reinforced plate |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012202379837U CN202607158U (en) | 2012-05-24 | 2012-05-24 | Adjustable welding jig for safety belt reinforced plate |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202607158U true CN202607158U (en) | 2012-12-19 |
Family
ID=47340890
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012202379837U Expired - Fee Related CN202607158U (en) | 2012-05-24 | 2012-05-24 | Adjustable welding jig for safety belt reinforced plate |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202607158U (en) |
Cited By (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103894768A (en) * | 2012-12-25 | 2014-07-02 | 上海龙钰电梯配件有限公司 | Elevator traction locomotive brake shoe machining clamp |
| CN104801872A (en) * | 2015-05-04 | 2015-07-29 | 河南鸿昌电子有限公司 | Semiconductor refrigeration piece welding machine |
| CN105414838A (en) * | 2015-11-30 | 2016-03-23 | 芜湖普威技研有限公司 | Workbench with welding clamp capable of being replaced |
| CN105436767A (en) * | 2015-12-16 | 2016-03-30 | 嵊州市银河铝业有限公司 | Welding machine applicable to production and processing of aluminium profiles |
| CN106141478A (en) * | 2016-08-29 | 2016-11-23 | 中国振华集团云科电子有限公司 | A kind of miniature parts end face welding equipment |
| CN107695591A (en) * | 2017-10-31 | 2018-02-16 | 马鞍山市盛力锁业科技有限公司 | One kind section fork linkage positioning clamping device |
| CN107962329A (en) * | 2017-10-31 | 2018-04-27 | 马鞍山市盛力锁业科技有限公司 | One kind section fork assembly clamping device |
| CN108333006A (en) * | 2018-01-09 | 2018-07-27 | 河海大学 | A kind of cuboid sample clamping device and its application method suitable for sizes |
| CN111889842A (en) * | 2020-08-06 | 2020-11-06 | 重庆电力高等专科学校 | Welding and assembling device for electronic and electrical devices |
| CN111906562A (en) * | 2019-05-27 | 2020-11-10 | 中车大同电力机车有限公司 | Car coupler clamping device |
| CN118559149A (en) * | 2024-07-03 | 2024-08-30 | 泰州巨环起重防护装备有限公司 | High altitude safety belt metal component welding equipment |
-
2012
- 2012-05-24 CN CN2012202379837U patent/CN202607158U/en not_active Expired - Fee Related
Cited By (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103894768A (en) * | 2012-12-25 | 2014-07-02 | 上海龙钰电梯配件有限公司 | Elevator traction locomotive brake shoe machining clamp |
| CN103894768B (en) * | 2012-12-25 | 2016-08-24 | 上海龙钰电梯配件有限公司 | A kind of elevator traction locomotive brake shoe clamp for machining |
| CN104801872A (en) * | 2015-05-04 | 2015-07-29 | 河南鸿昌电子有限公司 | Semiconductor refrigeration piece welding machine |
| CN104801872B (en) * | 2015-05-04 | 2017-04-05 | 河南鸿昌电子有限公司 | A kind of semiconductor refrigeration member bonding machine |
| CN105414838A (en) * | 2015-11-30 | 2016-03-23 | 芜湖普威技研有限公司 | Workbench with welding clamp capable of being replaced |
| CN105436767A (en) * | 2015-12-16 | 2016-03-30 | 嵊州市银河铝业有限公司 | Welding machine applicable to production and processing of aluminium profiles |
| CN106141478A (en) * | 2016-08-29 | 2016-11-23 | 中国振华集团云科电子有限公司 | A kind of miniature parts end face welding equipment |
| CN107962329A (en) * | 2017-10-31 | 2018-04-27 | 马鞍山市盛力锁业科技有限公司 | One kind section fork assembly clamping device |
| CN107695591A (en) * | 2017-10-31 | 2018-02-16 | 马鞍山市盛力锁业科技有限公司 | One kind section fork linkage positioning clamping device |
| CN108333006A (en) * | 2018-01-09 | 2018-07-27 | 河海大学 | A kind of cuboid sample clamping device and its application method suitable for sizes |
| CN108333006B (en) * | 2018-01-09 | 2020-06-02 | 河海大学 | Cubic sample clamping device suitable for various sizes and using method thereof |
| CN111906562A (en) * | 2019-05-27 | 2020-11-10 | 中车大同电力机车有限公司 | Car coupler clamping device |
| CN111889842A (en) * | 2020-08-06 | 2020-11-06 | 重庆电力高等专科学校 | Welding and assembling device for electronic and electrical devices |
| CN111889842B (en) * | 2020-08-06 | 2022-04-22 | 重庆电力高等专科学校 | Welding and assembling device for electronic and electrical devices |
| CN118559149A (en) * | 2024-07-03 | 2024-08-30 | 泰州巨环起重防护装备有限公司 | High altitude safety belt metal component welding equipment |
| CN118559149B (en) * | 2024-07-03 | 2024-11-29 | 泰州巨环起重防护装备有限公司 | High altitude safety belt metal component welding equipment |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204018958U (en) | A kind of multi-functional clamp for agitating friction welding | |
| CN205271248U (en) | Truck chassis tail lamp scaffold weldment frock | |
| CN202411719U (en) | Fixture for assembling and welding front end of underframe of railway vehicle | |
| CN204321407U (en) | Fin long slab radiator friction stir welding fixture | |
| CN201516541U (en) | Clamp for laser welding of battery shell | |
| CN204277210U (en) | A kind of friction stir welding universal fixturing | |
| CN102601569A (en) | Welding fixture for transverse side rod support assemblies | |
| CN203804585U (en) | Boring fixture for support of large mechanical travelling mechanism | |
| CN203401251U (en) | Adjustable welding jig | |
| CN106002038A (en) | Power battery base welding fixture | |
| CN108772658A (en) | Hollow type truck side sill with automatic centering clamping function welds displacement tool | |
| CN202143998U (en) | Clamp-based convex welding device | |
| CN205096783U (en) | H -beam location frock | |
| CN202639705U (en) | Special clamp for welding reinforcing plate of safety belt | |
| CN202701655U (en) | Welding clamp for transverse and lateral rod support assembly | |
| CN207668780U (en) | The abnormal workpieces welding tooling of upper and lower multi-angle formula | |
| CN203437828U (en) | Auxiliary welding device for external plate of car body | |
| CN202655842U (en) | L-shaped welding positioner and supporting and clamping device thereof | |
| CN205200885U (en) | Battery installation reinforcing plate fixture device | |
| CN211072226U (en) | A high-frequency welding system for side wall processing | |
| CN102950398B (en) | Welding device for elevator safety gear | |
| CN205834550U (en) | Power battery base welding fixture | |
| CN207577649U (en) | A kind of cross and the dual-purpose spot welding plank grip device of single-ride joint | |
| CN205798808U (en) | A kind of scalable welding localization tool | |
| CN205520189U (en) | Be used for two glib linkage distance devices of welding robot welding |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20121219 Termination date: 20150524 |
|
| EXPY | Termination of patent right or utility model |