CN202491045U - Crankshaft timing gear assembling device - Google Patents
Crankshaft timing gear assembling device Download PDFInfo
- Publication number
- CN202491045U CN202491045U CN2012201074719U CN201220107471U CN202491045U CN 202491045 U CN202491045 U CN 202491045U CN 2012201074719 U CN2012201074719 U CN 2012201074719U CN 201220107471 U CN201220107471 U CN 201220107471U CN 202491045 U CN202491045 U CN 202491045U
- Authority
- CN
- China
- Prior art keywords
- positioning
- pin
- crankshaft
- timing gear
- support
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images

Landscapes
- Gears, Cams (AREA)
Abstract
本实用新型涉及一种曲轴正时齿轮装配装置,其包括支撑定位盘、齿轮定位销、键槽定位销和若干个支撑销,所述支撑定位盘设有中心圆孔,中心圆孔上方设有一方槽,支撑定位盘端面上设有一定位孔,端面外圆设有若干个圆销孔,所述齿轮定位销安装在定位孔中,所述键槽定位销安装在方槽中,所述若干个支撑销安装在圆销孔中,其与正时齿轮的若干个齿间空当对应。装配时,将加热后的正时齿轮的定位孔对正齿轮定位销,齿间空当对正相应的支撑销,支撑定位盘上的中心圆孔对正曲轴小头圆柱,键槽定位销对正曲轴小头圆柱上的半圆键,沿曲轴小头圆柱向前推动支撑定位盘,将正时齿轮装入曲轴轴颈上。本实用新型结构合理,定位准确,操作简便,装配效率高。
The utility model relates to a crankshaft timing gear assembly device, which comprises a supporting positioning plate, a gear positioning pin, a keyway positioning pin and several supporting pins. The supporting positioning plate is provided with a central circular hole, and a square There is a positioning hole on the end surface of the support positioning plate, and several round pin holes are provided on the outer circle of the end surface. The gear positioning pin is installed in the positioning hole, the keyway positioning pin is installed in the square groove, and the several support The pins are installed in the round pin holes corresponding to the spaces between the teeth of the timing gear. When assembling, align the positioning hole of the heated timing gear with the alignment pin of the spur gear, align the gap between the teeth with the corresponding support pin, align the center hole on the support positioning plate with the small head cylinder of the crankshaft, and align the keyway positioning pin with the crankshaft The half-round key on the small end cylinder pushes the support positioning plate forward along the small end cylinder of the crankshaft, and the timing gear is packed on the crankshaft journal. The utility model has the advantages of reasonable structure, accurate positioning, convenient operation and high assembly efficiency.
Description
技术领域 technical field
本实用新型涉及曲轴齿轮装配领域,具体地说是一种曲轴正时齿轮装配装置。 The utility model relates to the field of crankshaft gear assembly, in particular to a crankshaft timing gear assembly device.
背景技术 Background technique
我们知道,正时齿轮是在机械装置中对完成相关控制功能起到时间尺度定位的齿轮。正时齿轮安装于发动机曲轴上,装配方法是将齿轮加热压入曲轴小头。由于它所处部位的工作特性,齿轮对曲轴连杆颈的周向位置要求很严格。为了保证安装位置的正确,通常在曲轴小头圆柱侧面设有半圆键槽,在正时齿轮侧面设有一定位孔,要求半圆键槽中心和正时齿轮中心都必须与曲轴第一连杆颈中心处在同一平面,要满足这种条件的装配非常困难。目前,市场上没有专用的曲轴正时齿轮装配装置,也没有这方面的文献报道。 We know that the timing gear is a gear that plays a time-scale positioning role in the completion of related control functions in a mechanical device. The timing gear is installed on the crankshaft of the engine, and the assembly method is to heat and press the gear into the small end of the crankshaft. Due to the working characteristics of its location, the gear has strict requirements on the circumferential position of the crank pin. In order to ensure the correct installation position, a semicircular keyway is usually provided on the side of the small cylinder of the crankshaft, and a positioning hole is provided on the side of the timing gear. It is very difficult to assemble the plane to meet this condition. At present, there is no special crankshaft timing gear assembly device on the market, and there is no literature report in this regard.
发明内容 Contents of the invention
本实用新型所要解决的技术问题是克服上述现有技术的不足,提供一种结构合理,定位准确,操作简便,装配效率高的曲轴正时齿轮装配装置。 The technical problem to be solved by the utility model is to overcome the deficiencies of the above-mentioned prior art and provide a crankshaft timing gear assembly device with reasonable structure, accurate positioning, easy operation and high assembly efficiency.
本实用新型解决上述技术问题采用的技术方案是:一种曲轴正时齿轮装配装置,其特征是:其包括支撑定位盘、齿轮定位销、键槽定位销和若干个支撑销,所述支撑定位盘设有中心圆孔,中心圆孔上方设有一方槽,支撑定位盘端面上设有一定位孔,端面外圆设有若干个圆销孔,所述齿轮定位销安装在定位孔中,其与正时齿轮上设有的定位孔对应;所述键槽定位销安装在方槽中,其与曲轴小头圆柱上设有的半圆键对应;所述若干个支撑销安装在圆销孔中,其与正时齿轮的若干个齿间空当对应。 The technical solution adopted by the utility model to solve the above technical problems is: a crankshaft timing gear assembly device, which is characterized in that it includes a support positioning plate, a gear positioning pin, a keyway positioning pin and several support pins, and the support positioning plate There is a central circular hole, a square groove is provided above the central circular hole, a positioning hole is provided on the end surface of the support positioning plate, and several round pin holes are provided on the outer circle of the end surface. The gear positioning pin is installed in the positioning hole, and it is aligned with the positive The positioning holes provided on the hour gear correspond; the keyway positioning pins are installed in the square grooves, which correspond to the semicircular keys provided on the small head cylinder of the crankshaft; the several support pins are installed in the round pin holes, which correspond to the The spaces between the teeth of the timing gear correspond to each other.
本实用新型所述支撑定位盘中心圆孔右上侧开有一与所述方槽贯通的“L”形切口。装配时,方便观察键槽定位销和半圆键的配合。 In the utility model, there is an "L"-shaped cutout connected with the square groove on the upper right side of the center hole of the support positioning plate. When assembling, it is convenient to observe the cooperation between the keyway positioning pin and the half-round key.
本实用新型所述键槽定位销后部为方形,前部为带止口的半圆形,与曲轴小头圆柱上的半圆键相对应配合定位。 The rear portion of the keyway locating pin described in the utility model is a square shape, and the front portion is a semicircle with a seam, which is correspondingly positioned with the semicircle key on the small head cylinder of the crankshaft.
本实用新型所述支撑定位盘端面外圆均布设有三个圆销孔,三个所述支撑销对应安装在圆销孔中,与正时齿轮的三个齿间空当对应。 According to the utility model, three round pin holes are evenly distributed on the outer circle of the end surface of the support positioning plate, and the three support pins are correspondingly installed in the round pin holes, corresponding to the spaces between the three teeth of the timing gear.
本实用新型装配使用时,将加热后的正时齿轮的定位孔对正齿轮定位销,若干个正时齿轮齿间空当对正相应的支撑销,正时齿轮靠紧支撑在支撑定位盘端面上,由安装在支撑定位盘上的支撑销、齿轮定位销支撑、定位。而后,手持支撑定位盘,将支撑定位盘上的中心圆孔对正曲轴小头圆柱,键槽定位销对正曲轴小头圆柱上的半圆键,沿曲轴小头圆柱向前推动支撑定位盘,将正时齿轮装入曲轴轴颈上,冷却后,实现曲轴正时齿轮的准确装配。对照现有技术,本实用新型结构合理,定位准确,操作简便,装配效率高,是一种理想的曲轴正时齿轮装配装置。 When the utility model is assembled and used, the positioning hole of the heated timing gear is aligned with the positioning pin of the timing gear, and the gaps between teeth of several timing gears are aligned with the corresponding support pins, and the timing gear is closely supported on the end surface of the supporting positioning plate. , supported and positioned by the support pin and the gear positioning pin installed on the support positioning plate. Then, hold the support positioning plate, align the central hole on the support positioning plate with the crankshaft small end cylinder, align the keyway positioning pin with the half-round key on the crankshaft small end cylinder, push the support positioning plate forward along the crankshaft small end cylinder, and The timing gear is installed on the crankshaft journal, and after cooling, the accurate assembly of the crankshaft timing gear is realized. Compared with the prior art, the utility model has the advantages of reasonable structure, accurate positioning, convenient operation and high assembly efficiency, and is an ideal crankshaft timing gear assembly device.
附图说明 Description of drawings
下面结合附图对本实用新型作进一步的描述。 Below in conjunction with accompanying drawing, the utility model is further described.
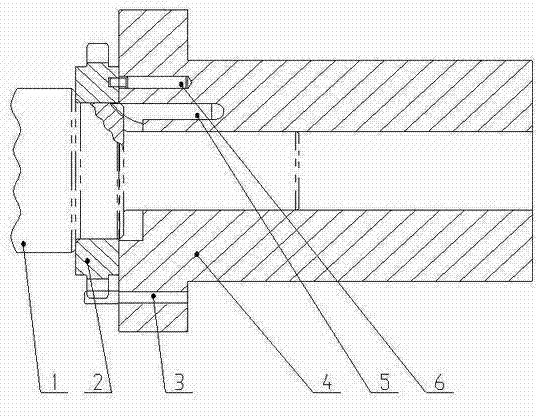
图1是本实用新型装配状态示意图。 Fig. 1 is a schematic diagram of the assembled state of the utility model.
图2是图1的左视示意图。 FIG. 2 is a schematic left view of FIG. 1 .
图中1.曲轴,2.正时齿轮,3.支撑销,4.支撑定位盘,5.键槽定位销,6.齿轮定位销。 Among the figure 1. crankshaft, 2. timing gear, 3. support pin, 4. support positioning plate, 5. keyway positioning pin, 6. gear positioning pin.
具体实施方式 Detailed ways
从图1和图2可以看出,一种曲轴正时齿轮装配装置,其用于将正时齿轮2装配到曲轴1上。同已有技术相同,正时齿轮2设有定位孔,曲轴1小头圆柱上设有半圆键,通过定位孔以及半圆键确定正时齿轮在曲轴上的准确安装位置。 It can be seen from FIG. 1 and FIG. 2 that a crankshaft timing gear assembly device is used for assembling the timing gear 2 onto the crankshaft 1 . Same as prior art, timing gear 2 is provided with positioning hole, and crankshaft 1 small head cylinder is provided with semicircle key, determines the accurate mounting position of timing gear on crankshaft by positioning hole and semicircle key.
本实用新型曲轴正时齿轮装配装置,其包括一支撑定位盘4、齿轮定位销6、键槽定位销5和若干个支撑销3。所述支撑定位盘4设有中心圆孔,中心圆孔上方设有一方槽,支撑定位盘4端面上设有一定位孔,端面外圆设有若干个圆销孔,所述齿轮定位销6安装在定位孔中,其与正时齿轮2上设有的定位孔对应;所述键槽定位销5安装在方槽中,其与曲轴1小头圆柱上设有的半圆键对应;所述若干个支撑销3安装在圆销孔中,其与正时齿轮2的若干个齿间空当对应。
The crankshaft timing gear assembly device of the present utility model comprises a supporting positioning plate 4, gear positioning pins 6,
本实用新型所述键槽定位销4是用于与曲轴1上半圆键配合定位而设置的。键槽定位销4后部为方形,前部为带止口的半圆形,与曲轴1小头圆柱上的半圆键相对应配合定位。 The keyway locating pin 4 described in the utility model is used for cooperating with the semicircle key on the crankshaft 1 to locate and arrange. The keyway locating pin 4 rear portion is square, and the front portion is a semicircle with seam, correspondingly cooperating with the semicircle key on the crankshaft 1 small end cylinder.
本实用新型所述支撑定位盘4中心圆孔右上侧开有一与所述方槽贯通的“L”形切口。装配时,可以从斜上方方便观察键槽定位销5和曲轴1小头圆柱上的半圆键的配合。
There is an "L" shaped cutout connected with the square groove on the upper right side of the central circular hole of the support positioning disc 4 in the utility model. During assembly, it is convenient to observe the cooperation of the keyway positioning
本实用新型所述支撑定位盘4上安装若干个支撑销3,支撑销3与正时齿轮2的对应齿间空当配合,起支撑正时齿轮的作用。一般来讲,安装三个支撑销3为最佳实施方式,具体是支撑定位盘4端面外圆相间120度,均布设有三个圆销孔,三个支撑销3分别对应安装在圆销孔中,与正时齿轮2的三个齿间空当对应,用来支撑托住正时齿轮。 Several support pins 3 are installed on the support positioning plate 4 described in the utility model, and the support pins 3 are matched with the corresponding interdental space of the timing gear 2 to play the role of supporting the timing gear. Generally speaking, installing three support pins 3 is the best implementation mode. Specifically, the outer circles of the end faces of the support positioning plate 4 are 120 degrees apart, and three round pin holes are evenly arranged, and the three support pins 3 are respectively installed in the round pin holes. , corresponding to the space between the three teeth of the timing gear 2, used to support and hold the timing gear.
本实用新型装配使用时,将加热后的正时齿轮2的定位孔对正齿轮定位销6,三个正时齿轮齿间空当对正相应的三个支撑销3,正时齿轮2靠紧支撑在支撑定位盘4端面上,由安装在支撑定位盘上的支撑销3、齿轮定位销6支撑、定位。而后,手持支撑定位盘4,将支撑定位盘4上的中心圆孔对正曲轴1小头圆柱,键槽定位销5对正曲轴1小头圆柱上的半圆键,沿曲轴小头圆柱向前推动支撑定位盘4,将正时齿轮2装入曲轴1轴颈上,冷却后,就完成了曲轴正时齿轮的准确装配。
When the utility model is assembled and used, the positioning hole of the heated timing gear 2 is aligned with the positioning pin 6 of the timing gear, and the spaces between the teeth of the three timing gears are aligned with the corresponding three support pins 3, and the timing gear 2 is closely supported. On the end face of the support positioning disc 4, it is supported and positioned by the support pin 3 and the gear positioning pin 6 installed on the support positioning disc. Then, hold the support positioning plate 4, align the center hole on the support positioning plate 4 with the crankshaft 1 small head cylinder,
本实用新型结构合理,定位准确,操作简便,装配效率高,是一种理想的曲轴正时齿轮装配装置。 The utility model has the advantages of reasonable structure, accurate positioning, convenient operation and high assembly efficiency, and is an ideal crankshaft timing gear assembly device.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012201074719U CN202491045U (en) | 2012-03-21 | 2012-03-21 | Crankshaft timing gear assembling device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2012201074719U CN202491045U (en) | 2012-03-21 | 2012-03-21 | Crankshaft timing gear assembling device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202491045U true CN202491045U (en) | 2012-10-17 |
Family
ID=46997288
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2012201074719U Expired - Fee Related CN202491045U (en) | 2012-03-21 | 2012-03-21 | Crankshaft timing gear assembling device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202491045U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102581548A (en) * | 2012-03-21 | 2012-07-18 | 天润曲轴股份有限公司 | Crankshaft timing gear assembling device |
| CN103802045A (en) * | 2012-11-07 | 2014-05-21 | 广西玉柴机器股份有限公司 | Crankshaft timing gear installing and positioning mechanism |
| CN103883456A (en) * | 2014-04-02 | 2014-06-25 | 广西玉柴机器股份有限公司 | Correcting device of timing pointer |
| CN110939718A (en) * | 2019-12-19 | 2020-03-31 | 一汽解放汽车有限公司 | A gear-driven integrally assembled dual-shaft balance shaft mechanism |
-
2012
- 2012-03-21 CN CN2012201074719U patent/CN202491045U/en not_active Expired - Fee Related
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102581548A (en) * | 2012-03-21 | 2012-07-18 | 天润曲轴股份有限公司 | Crankshaft timing gear assembling device |
| CN103802045A (en) * | 2012-11-07 | 2014-05-21 | 广西玉柴机器股份有限公司 | Crankshaft timing gear installing and positioning mechanism |
| CN103802045B (en) * | 2012-11-07 | 2016-02-24 | 广西玉柴机器股份有限公司 | Crankshaft timing gear installs detent mechanism |
| CN103883456A (en) * | 2014-04-02 | 2014-06-25 | 广西玉柴机器股份有限公司 | Correcting device of timing pointer |
| CN103883456B (en) * | 2014-04-02 | 2015-12-30 | 广西玉柴机器股份有限公司 | The correcting device of timing pointer |
| CN110939718A (en) * | 2019-12-19 | 2020-03-31 | 一汽解放汽车有限公司 | A gear-driven integrally assembled dual-shaft balance shaft mechanism |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102581548A (en) | Crankshaft timing gear assembling device | |
| CN201057064Y (en) | Engine camshaft gear timing alignment device | |
| CN103878533A (en) | Crankshaft and timing gear assembly device | |
| CN105058025A (en) | Portable type hydraulic bearing mounting and dismounting device | |
| CN102425497B (en) | Gas intake cone fixation structure of gas turbine engine | |
| CN106271589A (en) | A kind of assembling equipment for pre-installing valve rod, spring, pad | |
| CN201613518U (en) | Fixed tooling for engine assembly | |
| CN103111794A (en) | Novel crankshaft timing gear assembling device | |
| CN203547816U (en) | Camshaft fixing support structure | |
| CN205445686U (en) | Combination formula impeller structure of forked tail joggle | |
| CN201666183U (en) | A split flywheel housing | |
| CN105673085A (en) | Dovetail-joggled combined type impeller structure | |
| CN101863428B (en) | Tool special for assembling gas turbine pull rod-type rotor disc and using method thereof | |
| CN206717408U (en) | A kind of fan guard multistation automatic assembling machine | |
| CN204004183U (en) | Engine flywheel | |
| CN209025714U (en) | A kind of half iron camshaft assembly | |
| CN203738661U (en) | Press assembly fixture for catheter and seat ring of cylinder head | |
| CN207470249U (en) | A kind of cam shaft timing chain wheel | |
| CN210139086U (en) | A sheave installation structure | |
| CN203516678U (en) | Top cover gear shifting shaft positioning mechanism | |
| CN216541780U (en) | Assembly tool for oil pump of timing chain cover | |
| CN204728033U (en) | A kind of jacquard machine component rolling pulley body is optimized structure | |
| CN202480007U (en) | Assembly fixture for brake | |
| CN222727270U (en) | A valve needle fixing structure | |
| CN203130819U (en) | Connecting flange of transmission shaft |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20121017 Termination date: 20140321 |