CN115286416B - Production process of ceramic refrigerating sheet - Google Patents
Production process of ceramic refrigerating sheet Download PDFInfo
- Publication number
- CN115286416B CN115286416B CN202210965696.6A CN202210965696A CN115286416B CN 115286416 B CN115286416 B CN 115286416B CN 202210965696 A CN202210965696 A CN 202210965696A CN 115286416 B CN115286416 B CN 115286416B
- Authority
- CN
- China
- Prior art keywords
- vibrating screen
- copper particles
- vibrating
- ceramic
- mold
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B37/00—Joining burned ceramic articles with other burned ceramic articles or other articles by heating
- C04B37/02—Joining burned ceramic articles with other burned ceramic articles or other articles by heating with metallic articles
- C04B37/021—Joining burned ceramic articles with other burned ceramic articles or other articles by heating with metallic articles in a direct manner, e.g. direct copper bonding [DCB]
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07B—SEPARATING SOLIDS FROM SOLIDS BY SIEVING, SCREENING, SIFTING OR BY USING GAS CURRENTS; SEPARATING BY OTHER DRY METHODS APPLICABLE TO BULK MATERIAL, e.g. LOOSE ARTICLES FIT TO BE HANDLED LIKE BULK MATERIAL
- B07B1/00—Sieving, screening, sifting, or sorting solid materials using networks, gratings, grids, or the like
- B07B1/28—Moving screens not otherwise provided for, e.g. swinging, reciprocating, rocking, tilting or wobbling screens
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B07—SEPARATING SOLIDS FROM SOLIDS; SORTING
- B07B—SEPARATING SOLIDS FROM SOLIDS BY SIEVING, SCREENING, SIFTING OR BY USING GAS CURRENTS; SEPARATING BY OTHER DRY METHODS APPLICABLE TO BULK MATERIAL, e.g. LOOSE ARTICLES FIT TO BE HANDLED LIKE BULK MATERIAL
- B07B1/00—Sieving, screening, sifting, or sorting solid materials using networks, gratings, grids, or the like
- B07B1/46—Constructional details of screens in general; Cleaning or heating of screens
- B07B1/50—Cleaning
-
- C—CHEMISTRY; METALLURGY
- C04—CEMENTS; CONCRETE; ARTIFICIAL STONE; CERAMICS; REFRACTORIES
- C04B—LIME, MAGNESIA; SLAG; CEMENTS; COMPOSITIONS THEREOF, e.g. MORTARS, CONCRETE OR LIKE BUILDING MATERIALS; ARTIFICIAL STONE; CERAMICS; REFRACTORIES; TREATMENT OF NATURAL STONE
- C04B2237/00—Aspects relating to ceramic laminates or to joining of ceramic articles with other articles by heating
- C04B2237/30—Composition of layers of ceramic laminates or of ceramic or metallic articles to be joined by heating, e.g. Si substrates
- C04B2237/40—Metallic
- C04B2237/407—Copper
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02B—CLIMATE CHANGE MITIGATION TECHNOLOGIES RELATED TO BUILDINGS, e.g. HOUSING, HOUSE APPLIANCES OR RELATED END-USER APPLICATIONS
- Y02B30/00—Energy efficient heating, ventilation or air conditioning [HVAC]
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Ceramic Engineering (AREA)
- Materials Engineering (AREA)
- Structural Engineering (AREA)
- Organic Chemistry (AREA)
- Devices For Post-Treatments, Processing, Supply, Discharge, And Other Processes (AREA)
- Ceramic Products (AREA)
Abstract
本发明公开了一种陶瓷制冷片的生产工艺,包括振筛、压片、烧结和切割步骤,通过振筛模具放置于振筛机的振动框内,通过振动使铜颗粒对应进入振筛模具的每个凹模组内;振筛模具内设有若干个与单个瓷片铜颗粒位置大小匹配的凹模组,每个凹模内设有通孔;将振筛后带有铜颗粒的振筛模具放置于陶瓷基板上固定,然后通过下料机将铜颗粒覆于陶瓷基板上,下料机的下压板上设有与振筛模具上的通孔匹配的钢针,钢针穿过通孔将铜颗粒推出并覆于陶瓷基板上;最后进行烧结、切割,得到单个成品。本发明通过采用模具可将多个陶瓷制冷片同时覆铜,利用机械化操作,省时省力,质量稳定,减少了工作人员,提高了工作效率。
The invention discloses a production process of a ceramic refrigerating sheet, which includes the steps of vibrating sieve, tablet pressing, sintering and cutting. The vibrating sieve mold is placed in the vibrating frame of the vibrating sieve machine, and the copper particles are correspondingly entered into the vibrating sieve mold through vibration. In each concave mold group; the vibrating screen mold is provided with several concave mold groups matching the position and size of the copper particles of a single ceramic sheet, and each concave mold is provided with a through hole; the vibrating screen with copper particles after the vibrating screen The mold is placed on the ceramic substrate and fixed, and then the copper particles are covered on the ceramic substrate through the blanking machine. The lower platen of the blanking machine is provided with a steel needle matching the through hole on the vibrating screen mold, and the steel needle passes through the through hole The copper particles are pushed out and covered on the ceramic substrate; finally sintered and cut to obtain a single finished product. The present invention can simultaneously coat multiple ceramic refrigerating plates with copper by adopting a mould, utilizes mechanized operation, saves time and labor, has stable quality, reduces staff and improves work efficiency.
Description
技术领域technical field
本发明涉及一种陶瓷制冷片领域,具体涉及一种陶瓷制冷片的生产工艺。The invention relates to the field of ceramic refrigeration sheets, in particular to a production process of ceramic refrigeration sheets.
背景技术Background technique
目前,陶瓷制冷片也叫热电制冷片,不需要任何制冷剂,可连续工作,没有污染源没有旋转部件,不会发生反转效应,没有滑动部件,是一种固体片件,工作时没有震动、噪音、寿命长,安装简单。其具有两种功能,既能制冷,又能加热,制冷效率一般不高,但制热效率很高,永远大于1。因而使用一个片件就能够替代分立的加热系统和制冷系统。现有陶瓷制冷片的覆铜均是采用人工单个操作,费时费力,且质量不能得到高效统一。At present, ceramic cooling chips are also called thermoelectric cooling chips, which do not require any refrigerant and can work continuously. There is no pollution source, no rotating parts, no reversal effect, no sliding parts, and is a solid piece. There is no vibration, Noise, long life, simple installation. It has two functions, both cooling and heating. The cooling efficiency is generally not high, but the heating efficiency is very high, always greater than 1. It is thus possible to replace separate heating and cooling systems with one chip. The copper cladding of the existing ceramic refrigeration chips is all manually operated individually, which is time-consuming and laborious, and the quality cannot be efficiently unified.
发明内容Contents of the invention
本发明所要解决的技术问题是提供一种陶瓷制冷片的生产工艺,通过采用模具可将多个陶瓷制冷片同时覆铜,利用机械化操作,省时省力,质量稳定,减少了工作人员,提高了工作效率。The technical problem to be solved by the present invention is to provide a production process of ceramic refrigerating sheets. By using a mold, multiple ceramic refrigerating sheets can be coated with copper at the same time, and mechanized operation is used to save time and effort, and the quality is stable, reducing the number of workers and improving the production efficiency. work efficiency.
本发明解决技术问题所采用的技术方案是: 一种陶瓷制冷片的生产工艺,包括振筛、压片、烧结和切割步骤,具体工艺步骤如下,The technical solution adopted by the present invention to solve the technical problem is: a production process of ceramic refrigeration sheet, comprising the steps of vibrating screen, sheet pressing, sintering and cutting, and the specific process steps are as follows,
一、制作振筛模具:所述振筛模具包括矩形主体,所述矩形主体内设有若干个与单个瓷片铜颗粒位置大小匹配的凹模组,每个凹模内设有通孔,通孔贯穿整个矩形主体;1. Making the vibrating sieve mold: the vibrating sieve mold includes a rectangular main body, and the rectangular main body is provided with several concave mold groups matching the position and size of a single ceramic sheet copper particle, and each concave mold is provided with a through hole through which The hole runs through the entire rectangular body;
二、振筛:将若干振筛模具固定于振筛机的振动框内,通过振动使铜颗粒对应进入振筛模具的每个凹模组内;2. Vibrating screen: Fix several vibrating screen molds in the vibrating frame of the vibrating screen machine, and make copper particles enter into each concave mold group of the vibrating screen mold through vibration;
三、压片:将带有铜颗粒的振筛模具放置于陶瓷基板上固定,然后通过下料机将铜颗粒覆于陶瓷基板上,所述下料机上设有下压板,下压板上设有与振筛模具上的通孔匹配的钢针,钢针穿过通孔将铜颗粒推出并覆于陶瓷基板上;3. Tablet pressing: Place the vibrating screen mold with copper particles on the ceramic substrate and fix it, and then cover the copper particles on the ceramic substrate through the blanking machine. A steel needle matching the through hole on the vibrating screen mold, the steel needle passes through the through hole to push the copper particles out and cover the ceramic substrate;
四、烧结:将覆有铜颗粒的陶瓷基板叠放于3~5层支架内,放入烧结箱烧结;4. Sintering: stack the ceramic substrate covered with copper particles in 3 to 5 layers of brackets, put them into a sintering box for sintering;
五、切割:将烧结好的陶瓷基板进行切割,即得到单个成品。5. Cutting: cutting the sintered ceramic substrate to obtain a single finished product.
作为一种优选,所述振筛机包括电机底座和两个振动框,所述振动框内可放置两块振筛模具。As a preference, the vibrating screen machine includes a motor base and two vibrating frames, and two vibrating screen molds can be placed in the vibrating frames.
作为一种优选,所述下料机包括底座、下压气缸和下压板,通过下压气缸将下压板上的钢针穿入通孔,将铜颗粒推出覆于陶瓷基板上。As a preference, the blanking machine includes a base, a down-pressing cylinder and a down-pressing plate, through which the steel needle on the down-pressing plate is penetrated into the through hole, and the copper particles are pushed out and covered on the ceramic substrate.
作为一种优选,所述矩形主体内设有16~54个与单个瓷片铜颗粒位置大小匹配的凹模组,每个凹模的槽深为0.3mm。As a preference, 16 to 54 concave mold groups matching the position and size of a single tile copper particle are arranged in the rectangular body, and the groove depth of each concave mold is 0.3mm.
本发明是电流换能型片件,经过输入电流的控制,可完成高精度的温度控制,再加上温度检测和控制手法,很简单完成遥控、程控、计算机控制,便于组成自动控制系统。产品热惯性十分小,制冷制热时刻很快,在热端散热良好冷端空载的情况下,通电不到一分钟,就能达到最大温差。产品单个制冷元件对的效率很小,但组合成电堆,用同类型的电堆串、并联的办法组合成制冷系统的话,效率就能够做的很大,因而制冷效率能够做到几毫瓦到上万瓦的范围。产品温差范围大,从正温90℃到负温度130℃都能够完成。The present invention is a current transduction type piece, through the control of the input current, it can complete high-precision temperature control, coupled with temperature detection and control methods, it is very simple to complete remote control, program control, and computer control, and it is convenient to form an automatic control system. The thermal inertia of the product is very small, and the cooling and heating time is very fast. In the case of good heat dissipation at the hot end and no load at the cold end, the maximum temperature difference can be reached in less than one minute after power on. The efficiency of a single pair of cooling elements of the product is very small, but if they are combined into a stack, and the same type of stacks are combined in series or parallel to form a refrigeration system, the efficiency can be made very high, so the cooling efficiency can reach several milliwatts to tens of thousands of watts. The temperature range of the product is large, and it can be completed from a positive temperature of 90°C to a negative temperature of 130°C.
本发明的有益效果是: 通过采用模具可将多个陶瓷制冷片同时覆铜,利用机械化操作,省时省力,质量稳定,减少了工作人员,提高了工作效率。The beneficial effects of the present invention are: by adopting the mould, a plurality of ceramic refrigerating plates can be coated with copper at the same time, and mechanized operation is used to save time and labor, and the quality is stable, reducing the number of workers and improving work efficiency.
附图说明Description of drawings
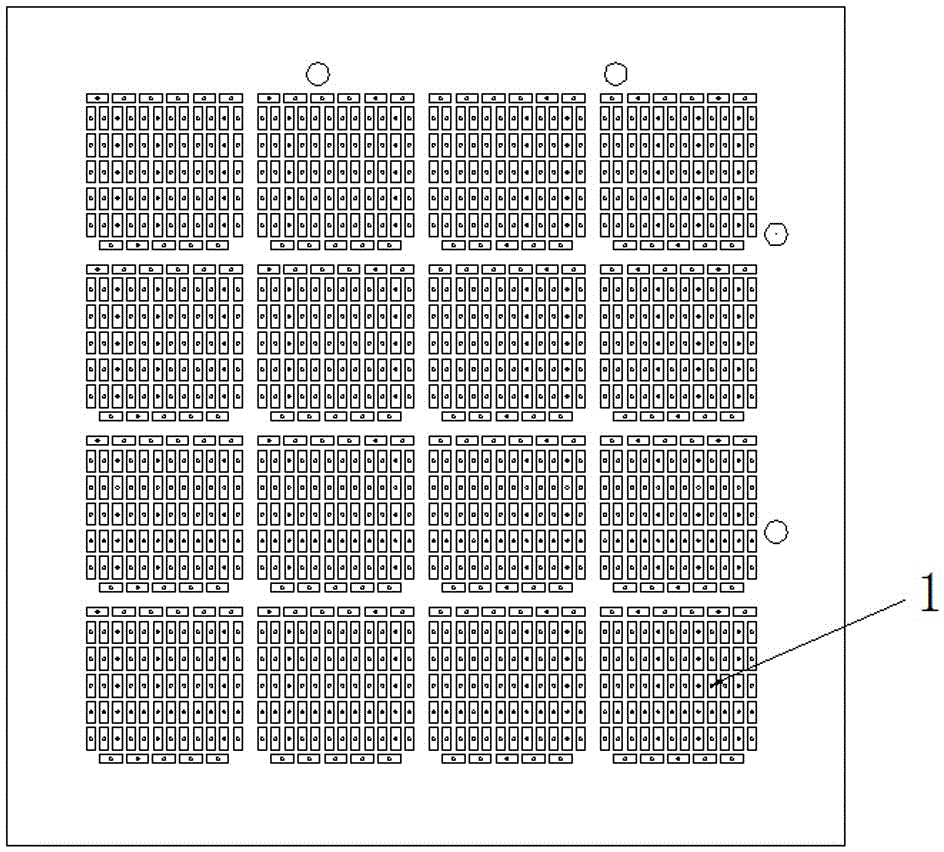
图1为本发明实施例振筛模具的结构示意图。Fig. 1 is a structural schematic diagram of a vibrating screen mold according to an embodiment of the present invention.
图2为本发明实施例凹模组的结构示意图。Fig. 2 is a schematic structural diagram of a die set according to an embodiment of the present invention.
图3为本发明实施例振筛机的结构示意图。Fig. 3 is a structural schematic diagram of a vibrating screen machine according to an embodiment of the present invention.
图4为本发明实施例下料机的主视示意图。Fig. 4 is a schematic front view of a blanking machine according to an embodiment of the present invention.
图5为本发明实施例下料机的左视示意图。Fig. 5 is a schematic left view of the blanking machine according to the embodiment of the present invention.
其中,1. 凹模组;2. 凹模;3. 通孔;4. 振动框;5. 下压板;6. 底座;7. 下压气缸;8. 工作平台;9. 电机底座。Among them, 1. Die group; 2. Die; 3. Through hole; 4. Vibration frame; 5. Lower pressure plate; 6. Base; 7. Lower pressure cylinder; 8. Working platform;
下面结合附图对本发明做进一步说明。The present invention will be further described below in conjunction with the accompanying drawings.
具体实施方式Detailed ways
实施例1: 一种陶瓷制冷片的生产工艺,包括振筛、压片、烧结和切割步骤,具体工艺步骤如下,Embodiment 1: A kind of production technology of ceramic refrigerating plate, comprises vibrating screen, pressing tablet, sintering and cutting steps, and concrete process step is as follows,
一、制作振筛模具:如图1、图2所示,所述振筛模具包括矩形主体,所述矩形主体内设有16个与单个瓷片铜颗粒位置大小匹配的凹模组1,每个凹模2内设有通孔3,通孔3贯穿整个矩形主体,每个凹模的槽深为0.3mm;One, make vibrating sieve mould: as shown in Fig. 1, Fig. 2, described vibrating sieve mold comprises rectangular main body, and described rectangular main body is provided with 16
二、振筛:将若干振筛模具固定于振筛机的振动框4内,如图3所示,所述振筛机包括电机底座9和两个振动框4,所述振动框4内可放置两块振筛模具,通过振动使铜颗粒对应进入振筛模具的每个凹模组1内;Two, vibrating screen: some vibrating screen molds are fixed in the vibrating
三、压片:将带有铜颗粒的振筛模具放置于陶瓷基板上固定,然后放置于下料机的工作平台8上,如图4、图5所示,所述下料机包括底座6、下压气缸7和下压板5,下压板5上设有与振筛模具上的通孔3匹配的钢针,通过下压气缸7将下压板上5的钢针穿入通孔3,将铜颗粒推出覆于陶瓷基板上;3. Tablet pressing: Place the vibrating screen mold with copper particles on the ceramic substrate and fix it, and then place it on the working
四、烧结:将覆有铜颗粒的陶瓷基板叠放于3层支架内,放入烧结箱烧结;Four, sintering: stack the ceramic substrate covered with copper particles in a 3-layer support, put it into a sintering box for sintering;
五、切割:将烧结好的陶瓷基板进行切割,即得到单个成品。5. Cutting: cutting the sintered ceramic substrate to obtain a single finished product.
本发明中振筛机和下料机底座中均设控制系统,可对一系列相关参数进行设置。Both the vibrating screen machine and the feeder base of the present invention are equipped with a control system, which can set a series of related parameters.
实施例2:第二种陶瓷制冷片的生产工艺,包括振筛、压片、烧结和切割步骤,具体工艺步骤如下,Embodiment 2: the production technology of the second kind of ceramic refrigerating sheet, comprises vibrating sieve, tabletting, sintering and cutting steps, and concrete process step is as follows,
一、制作振筛模具:所述振筛模具包括矩形主体,所述矩形主体内设有24个与单个瓷片铜颗粒位置大小匹配的凹模组1,每个凹模2内设有通孔3,通孔3贯穿整个矩形主体,每个凹模的槽深为0.3mm;1. Making the vibrating screen mold: the vibrating screen mold includes a rectangular main body, and the rectangular main body is provided with 24
四、烧结:将覆有铜颗粒的陶瓷基板叠放于4层支架内,放入烧结箱烧结。4. Sintering: stack the ceramic substrate covered with copper particles in a 4-layer support, put it into a sintering box for sintering.
其它与实施例1相同。Others are the same as in Example 1.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210965696.6A CN115286416B (en) | 2022-08-12 | 2022-08-12 | Production process of ceramic refrigerating sheet |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210965696.6A CN115286416B (en) | 2022-08-12 | 2022-08-12 | Production process of ceramic refrigerating sheet |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115286416A CN115286416A (en) | 2022-11-04 |
| CN115286416B true CN115286416B (en) | 2023-06-09 |
Family
ID=83827549
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202210965696.6A Active CN115286416B (en) | 2022-08-12 | 2022-08-12 | Production process of ceramic refrigerating sheet |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115286416B (en) |
Citations (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1352688A (en) * | 1963-04-09 | 1964-02-14 | Schuechtermann & Kremer | Vibrating resonance screen |
| FR2013892A1 (en) * | 1968-07-29 | 1970-04-10 | Kipp Robert | |
| JP2002016161A (en) * | 2000-06-27 | 2002-01-18 | Sumitomo Metal Electronics Devices Inc | Package component, manufacturing method therefor and method for sealing package using the package component |
| JP2005045143A (en) * | 2003-07-25 | 2005-02-17 | Murata Mfg Co Ltd | Method for manufacturing ceramic substrate with projection electrode |
| JP2016064963A (en) * | 2014-09-26 | 2016-04-28 | Toto株式会社 | Ceramic molded body and method for producing the same |
| JP2017005182A (en) * | 2015-06-15 | 2017-01-05 | 株式会社アイン | Method for manufacturing ceramic wiring board |
| CN206935765U (en) * | 2017-07-10 | 2018-01-30 | 汤朱雄 | A kind of aquatic products device for vibration screening |
| CN209161864U (en) * | 2018-09-13 | 2019-07-26 | 广东风华高新科技股份有限公司 | A sintered block with copper particles attached |
| CN210788092U (en) * | 2019-09-02 | 2020-06-19 | 江苏华光新材料科技有限公司 | Powder coating's device that sieves for coiled material |
| CN210906840U (en) * | 2019-11-21 | 2020-07-03 | 青岛岳石新能源科技有限公司 | Scale graphite refines screening installation |
| CN212633368U (en) * | 2020-04-28 | 2021-03-02 | 扬州中欣高分子材料有限公司 | A vibrating screen for screening plastic particles |
| CN213727736U (en) * | 2020-11-14 | 2021-07-20 | 山东蓝澳环保科技有限公司 | Jarring formula sieving machine |
| CN114464539A (en) * | 2021-07-27 | 2022-05-10 | 井敏 | Manufacturing method for metallizing through hole of ceramic substrate |
| CN114464726A (en) * | 2022-01-26 | 2022-05-10 | 浙江精瓷半导体有限责任公司 | Convenient and quick arrangement device and process for refrigeration sheets |
| CN114709324A (en) * | 2022-02-15 | 2022-07-05 | 河南省科学院应用物理研究所有限公司 | High-reliability thermoelectric refrigerating chip and packaging method thereof |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5526867A (en) * | 1988-11-10 | 1996-06-18 | Lanxide Technology Company, Lp | Methods of forming electronic packages |
| JP3896273B2 (en) * | 2001-10-29 | 2007-03-22 | タニコー株式会社 | Sieve device |
| US7654394B2 (en) * | 2004-06-14 | 2010-02-02 | Action Equipment Company, Inc. | Flexible mat screening or conveying apparatus |
| CN206083064U (en) * | 2016-08-24 | 2017-04-12 | 何建慧 | Yellow mud sieve separator |
| CN113413368A (en) * | 2021-07-15 | 2021-09-21 | 佛山市隆信医药科技有限公司 | Preparation process of pellets or granules |
| CN216778902U (en) * | 2021-11-30 | 2022-06-21 | 后英集团海城市水泉滑石矿有限公司 | Sieving mechanism is smashed to talcum powder |
-
2022
- 2022-08-12 CN CN202210965696.6A patent/CN115286416B/en active Active
Patent Citations (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1352688A (en) * | 1963-04-09 | 1964-02-14 | Schuechtermann & Kremer | Vibrating resonance screen |
| FR2013892A1 (en) * | 1968-07-29 | 1970-04-10 | Kipp Robert | |
| JP2002016161A (en) * | 2000-06-27 | 2002-01-18 | Sumitomo Metal Electronics Devices Inc | Package component, manufacturing method therefor and method for sealing package using the package component |
| JP2005045143A (en) * | 2003-07-25 | 2005-02-17 | Murata Mfg Co Ltd | Method for manufacturing ceramic substrate with projection electrode |
| JP2016064963A (en) * | 2014-09-26 | 2016-04-28 | Toto株式会社 | Ceramic molded body and method for producing the same |
| JP2017005182A (en) * | 2015-06-15 | 2017-01-05 | 株式会社アイン | Method for manufacturing ceramic wiring board |
| CN206935765U (en) * | 2017-07-10 | 2018-01-30 | 汤朱雄 | A kind of aquatic products device for vibration screening |
| CN209161864U (en) * | 2018-09-13 | 2019-07-26 | 广东风华高新科技股份有限公司 | A sintered block with copper particles attached |
| CN210788092U (en) * | 2019-09-02 | 2020-06-19 | 江苏华光新材料科技有限公司 | Powder coating's device that sieves for coiled material |
| CN210906840U (en) * | 2019-11-21 | 2020-07-03 | 青岛岳石新能源科技有限公司 | Scale graphite refines screening installation |
| CN212633368U (en) * | 2020-04-28 | 2021-03-02 | 扬州中欣高分子材料有限公司 | A vibrating screen for screening plastic particles |
| CN213727736U (en) * | 2020-11-14 | 2021-07-20 | 山东蓝澳环保科技有限公司 | Jarring formula sieving machine |
| CN114464539A (en) * | 2021-07-27 | 2022-05-10 | 井敏 | Manufacturing method for metallizing through hole of ceramic substrate |
| CN114464726A (en) * | 2022-01-26 | 2022-05-10 | 浙江精瓷半导体有限责任公司 | Convenient and quick arrangement device and process for refrigeration sheets |
| CN114709324A (en) * | 2022-02-15 | 2022-07-05 | 河南省科学院应用物理研究所有限公司 | High-reliability thermoelectric refrigerating chip and packaging method thereof |
Non-Patent Citations (1)
| Title |
|---|
| 0.12mm筛孔单振源共振筛工艺效果试验分析;赵环帅;黄勇;李准;;矿山机械(第01期);全文 * |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115286416A (en) | 2022-11-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110834095A (en) | A method for selective laser melting to form dense-loose integrated mold parts | |
| CN107591336B (en) | A method for preparing a cavity structure of a low-temperature co-fired ceramic substrate | |
| CN115286416A (en) | A kind of production process of ceramic refrigeration sheet | |
| CN209923186U (en) | hot bending die | |
| CN120773373A (en) | Linear hot-pressing circulation equipment and process | |
| CN209408656U (en) | A PCB inverted extrusion flat one-time forming stamping die | |
| CN201303466Y (en) | Off-line circuit substrate rapid processing die | |
| CN111873381A (en) | Improved diaphragm high-pressure forming die | |
| CN207677024U (en) | A kind of hot cold-press reshaping machine of battery core | |
| CN212528654U (en) | Improved diaphragm high-pressure forming die | |
| CN217703864U (en) | Variable thickness batch production's mould | |
| CN201015890Y (en) | Insulating brick production equipment | |
| CN221734808U (en) | Copper powder ring sintering jig and sintering equipment | |
| CN220543928U (en) | Lamination mold | |
| CN108218199A (en) | A kind of molding die of tetra- side hot bending products of 3D | |
| CN224210356U (en) | Sound diaphragm hot briquetting machine | |
| CN224103651U (en) | Corrugated board hot-pressing laminating machine | |
| CN100509339C (en) | Optical plate forming system and process thereof | |
| CN214645820U (en) | A kind of anti-skid pressing device for hot press forming machine | |
| CN223819568U (en) | An isothermal forging die tooling for manufacturing titanium alloy lower crossarm | |
| CN213500390U (en) | SPC floor hot briquetting pilot plant | |
| CN223197984U (en) | Forging device for high-temperature alloy plate blank difficult to deform | |
| CN216441530U (en) | Automatic feeding device for hot press | |
| CN201364825Y (en) | Encapsulation die for dye-sensitized solar battery | |
| CN110293687B (en) | Polyetherimide multi-manifold plate bonding method |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| PP01 | Preservation of patent right | ||
| PP01 | Preservation of patent right |
Effective date of registration: 20250828 Granted publication date: 20230609 |