CN102501101A - Clamp body for machining side plate of pulley frame, and method for machining and positioning side plate of pulley frame - Google Patents
Clamp body for machining side plate of pulley frame, and method for machining and positioning side plate of pulley frame Download PDFInfo
- Publication number
- CN102501101A CN102501101A CN2011103241805A CN201110324180A CN102501101A CN 102501101 A CN102501101 A CN 102501101A CN 2011103241805 A CN2011103241805 A CN 2011103241805A CN 201110324180 A CN201110324180 A CN 201110324180A CN 102501101 A CN102501101 A CN 102501101A
- Authority
- CN
- China
- Prior art keywords
- positioning
- side plate
- pulley frame
- hole
- clamp body
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 15
- 238000003754 machining Methods 0.000 title claims abstract description 14
- 238000003825 pressing Methods 0.000 claims abstract description 9
- 238000009434 installation Methods 0.000 claims abstract description 7
- 238000005516 engineering process Methods 0.000 claims description 6
- 238000010586 diagram Methods 0.000 description 4
- 238000004519 manufacturing process Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000005266 casting Methods 0.000 description 1
- 238000003801 milling Methods 0.000 description 1
- 239000013585 weight reducing agent Substances 0.000 description 1
Images


Landscapes
- Jigs For Machine Tools (AREA)
Abstract
本发明公开了一种用于加工滑轮架侧板的夹具体,夹具体的上表面为工作面,沿夹具体的上表面纵轴两边设置有对称的台阶和多个定位安装用的孔,两个台阶之间设置有短通槽,短通槽的底面为一段定位面,在定位面上开有一个台阶孔,台阶孔的上段是光孔,台阶孔的下段是螺纹孔。本发明还公开了利用前述的夹具体对滑轮架侧板进行加工定位方法,粗加工时以侧板下边的四个圆台为定位支撑面,采用多点定位,压板压紧方式;精加工时为防止变形采用“一点定位”,减少了变形及误差;左右件在同一个工装上完成,加工精度高,配合精度好。
The invention discloses a clamping body for processing the side plate of a pulley frame. The upper surface of the clamping body is a working surface, and symmetrical steps and a plurality of holes for positioning and installation are arranged along both sides of the longitudinal axis of the upper surface of the clamping body. A short through groove is arranged between the two steps, the bottom surface of the short through groove is a section of positioning surface, and a stepped hole is opened on the positioning surface, the upper section of the stepped hole is a smooth hole, and the lower section of the stepped hole is a threaded hole. The invention also discloses a method for processing and positioning the side plate of the pulley frame by using the aforementioned clamp body. During rough machining, the four round tables under the side plate are used as positioning support surfaces, and multi-point positioning is adopted, and the pressing plate is pressed; "One-point positioning" is used to prevent deformation, which reduces deformation and errors; the left and right parts are completed on the same tooling, with high processing accuracy and good matching accuracy.
Description
技术领域 technical field
本发明属于机械设备制造技术领域,涉及一种用于加工滑轮架侧板的夹具体,本发明还涉及一种利用该夹具体进行滑轮架侧板的加工定位方法。The invention belongs to the technical field of mechanical equipment manufacturing, and relates to a clamping body for processing the side plate of a pulley frame, and also relates to a method for processing and positioning the side plate of a pulley frame by using the clamping body.
背景技术 Background technique
滑轮架是飞机空投装置中的一个重要部件,滑轮架侧板包括左侧板、右侧板组成,左、右侧板在结构上对称,使用时配对使用,属于大尺寸的薄壁异形件,厚度不均匀,形状复杂,尺寸精度要求较高。The pulley frame is an important part of the aircraft airdrop device. The side plate of the pulley frame consists of a left side plate and a right side plate. The left and right side plates are symmetrical in structure. When used in pairs, they are large-sized thin-walled special-shaped parts. The thickness is uneven, the shape is complex, and the dimensional accuracy is high.
现有技术采用常规的多点定位和装夹方法进行加工时,由于无法克服应力集中的问题,会导致滑轮架侧板变形,很难保证滑轮架侧板的技术要求。左右件由于存在加工精度差,导致配合精度不好。In the prior art, when conventional multi-point positioning and clamping methods are used for processing, the problem of stress concentration cannot be overcome, which will lead to deformation of the side plate of the pulley frame, and it is difficult to ensure the technical requirements of the side plate of the pulley frame. Due to the poor processing accuracy of the left and right parts, the matching accuracy is not good.
发明内容 Contents of the invention
本发明的目的是提供一种用于加工滑轮架侧板的夹具体,解决了现有技术滑轮架侧板加工时没有专用设备,在普通台架上加工后应力集中,变形大的问题。The purpose of the present invention is to provide a clamping body for processing the side plate of the pulley frame, which solves the problems of the prior art that there is no special equipment for processing the side plate of the pulley frame, and the problems of stress concentration and large deformation after processing on a common bench are solved.
本发明的另一目的是提供一种利用前述的夹具体对滑轮架侧板的加工定位方法。Another object of the present invention is to provide a method for processing and positioning the side plate of the pulley frame by using the aforementioned clamp body.
本发明所采用的技术方案是:一种用于加工滑轮架侧板的夹具体,夹具体的上表面为工作面,沿夹具体的上表面纵轴两边设置有对称的台阶和许多定位安装用的孔,两个台阶之间设置有短通槽,短通槽的底面为一段定位面,在定位面上开有一个台阶孔,台阶孔的上段是光孔,台阶孔的下段是螺纹孔。The technical solution adopted in the present invention is: a clamping body for processing the side plate of the pulley frame, the upper surface of the clamping body is a working surface, and symmetrical steps and many positioning installations are arranged along both sides of the longitudinal axis of the upper surface of the clamping body. A short through groove is arranged between the two steps, the bottom surface of the short through groove is a positioning surface, and a step hole is opened on the positioning surface, the upper part of the step hole is a smooth hole, and the lower part of the step hole is a threaded hole.
本发明所采用的另一技术方案是:一种利用上述的装置进行滑轮架侧板的加工定位方法,利用一种装置,其结构是,夹具体的上表面为工作面,沿夹具体的上表面纵轴两边设置有对称的台阶和许多定位安装用的孔,两个台阶之间设置有短通槽,短通槽的底面为一段定位面,在定位面上开有一个台阶孔,台阶孔的上段是光孔,台阶孔的下段是螺纹孔;夹具体的上表面设置有多个压板、辅助夹具A和辅助夹具B,Another technical solution adopted by the present invention is: a method for processing and positioning the side plate of the pulley frame using the above-mentioned device, using a device whose structure is that the upper surface of the clamp body is the working surface, and the upper surface of the clamp body along the There are symmetrical steps and many holes for positioning and installation on both sides of the longitudinal axis of the surface. There is a short through groove between the two steps. The bottom surface of the short through groove is a positioning surface. There is a step hole on the positioning surface. The step hole The upper part of the step hole is a light hole, and the lower part of the step hole is a threaded hole; the upper surface of the clamp body is provided with a plurality of pressure plates, auxiliary fixture A and auxiliary fixture B,
先将夹具体固定在机床的工作台上,再将需要加工的滑轮架侧板的光面放置在夹具体短通槽的定位面上,按照以下步骤实施:First fix the clamp body on the workbench of the machine tool, and then place the smooth surface of the side plate of the pulley frame to be processed on the positioning surface of the short through groove of the clamp body, and implement according to the following steps:
第一步,采用多点定位进行粗加工,即用多个支撑钉对滑轮架侧板光面四个支撑面进行支撑定位,通过螺钉将压板压紧在台阶上,通过辅助夹具A和辅助夹具B对滑轮架侧板两端部位进行定位,各个压板和辅助夹具的压紧端同时将滑轮架侧板压紧在定位面上,按照加工工艺实施粗加工;The first step is to use multi-point positioning for rough machining, that is, use multiple support nails to support and position the four support surfaces of the smooth surface of the side plate of the pulley frame, press the pressure plate on the step with screws, and use auxiliary fixture A and auxiliary fixture B. Position the two ends of the side plate of the pulley frame, and press the side plate of the pulley frame against the positioning surface at the same time by the pressing ends of each pressing plate and auxiliary fixture, and carry out rough machining according to the processing technology;
第二步,采用一点定位进行精加工,利用四个支撑钉在滑轮架侧板的四个角上分别进行辅助支撑,在滑轮架侧板的装配孔中套入定位套,将圆形压板压在定位套上端口,将螺栓套进定位套及定位面的台阶孔中,将滑轮架侧板压紧在定位面上,按照加工工艺实施精加工。The second step is to use one-point positioning for finishing, using four supporting nails to provide auxiliary support on the four corners of the side plate of the pulley frame, and insert a positioning sleeve into the assembly hole of the side plate of the pulley frame, and press the circular pressure plate At the upper port of the positioning sleeve, insert the bolts into the step holes of the positioning sleeve and the positioning surface, press the side plate of the pulley frame against the positioning surface, and perform finishing according to the processing technology.
本发明的有益效果是:该加工夹具体结构简单,便于制作,使用方便,该方法在滑轮架左右侧板加工过程中,通过“多点定位”及“一点定位”减少了滑轮架侧板加工中的变形及误差;左右件在同一个工装上完成,加工精度高、配合精度好。The beneficial effects of the present invention are: the processing clamp has a simple structure, is easy to manufacture, and is convenient to use. In the process of processing the left and right side plates of the pulley frame, the method reduces the processing of the side plates of the pulley frame through "multi-point positioning" and "one-point positioning". The deformation and error in the process; the left and right parts are completed on the same tooling, with high processing accuracy and good matching accuracy.
附图说明 Description of drawings
图1是本发明的滑轮架侧板夹具体的工作面结构示意图;Fig. 1 is the working face structure schematic diagram of pulley frame side plate clamping body of the present invention;
图2是本发明的滑轮架侧板夹具体的背面结构示意图;Fig. 2 is the back structure schematic diagram of pulley frame side plate clip body of the present invention;
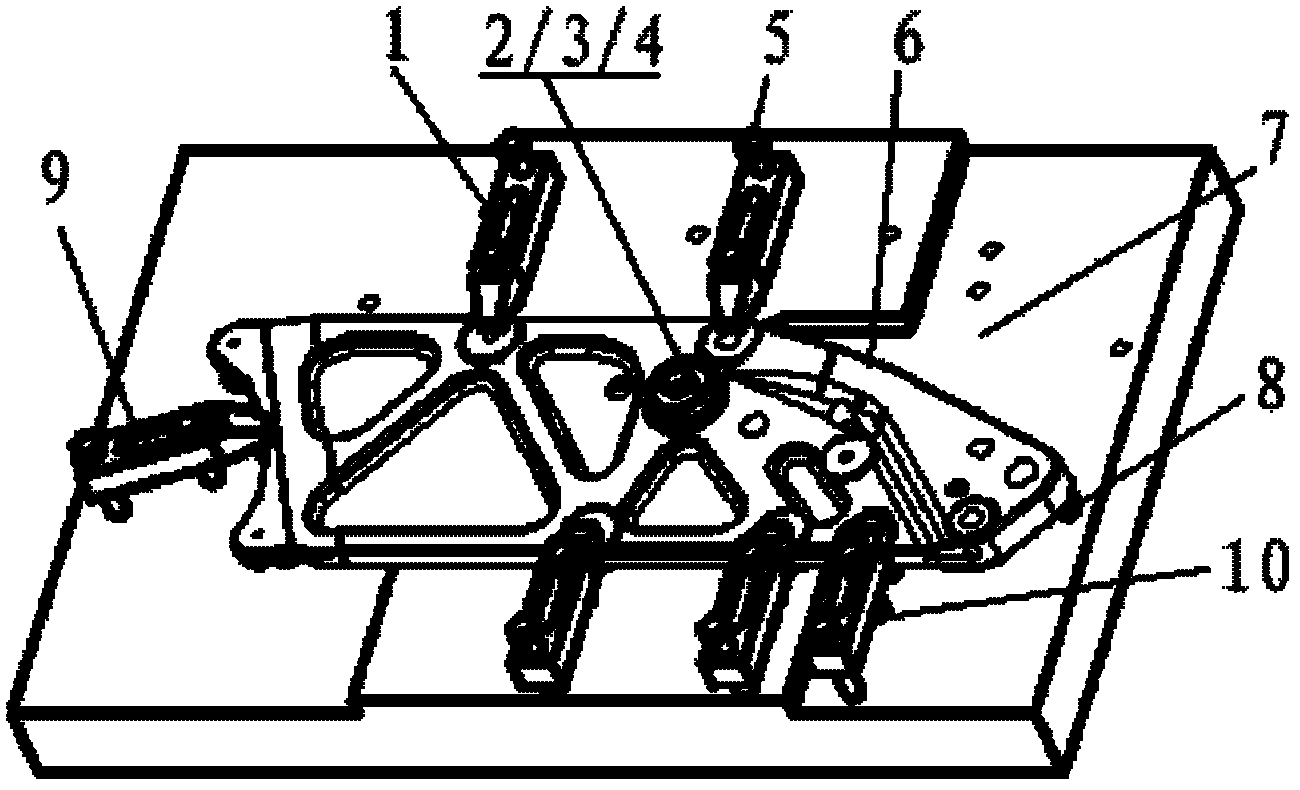
图3是本发明方法中的滑轮架侧板在夹具体上的安装示意图;Fig. 3 is the schematic diagram of the installation of the pulley frame side plate on the clamp body in the method of the present invention;
图4是本发明方法中的滑轮架侧板与夹具体装配的俯视图;Fig. 4 is the top view of pulley frame side plate and clip body assembly in the inventive method;
图5是图4中的A-A方向截面示意图。Fig. 5 is a schematic cross-sectional view along the A-A direction in Fig. 4 .
图中,1.压板,2.螺栓,3.圆形压板,4.定位套,5.螺钉,6.滑轮架侧板,7.夹具体,8.支撑钉,9.辅助夹具A,10.辅助夹具B,11.定位面,12.台阶孔,13.台阶,14.孔。In the figure, 1. Press plate, 2. Bolt, 3. Round press plate, 4. Positioning sleeve, 5. Screw, 6. Pulley frame side plate, 7. Clamp body, 8. Support nail, 9. Auxiliary fixture A, 10 .Auxiliary fixture B, 11. Positioning surface, 12. Step hole, 13. Step, 14. Hole.
具体实施方式 Detailed ways
下面结合附图和具体实施方式对本发明进行详细说明。The present invention will be described in detail below in conjunction with the accompanying drawings and specific embodiments.
图1、图2是本发明的用于加工滑轮架侧板的夹具体7的上下表面结构示意图,夹具体7制作为一个铸件,上表面为工作面,沿上表面纵轴两边设置有对称的台阶13和许多定位安装用的孔14,两个台阶13之间设置有短通槽,短通槽的底面为一段精度较高的定位面11,在定位面11上开有一个台阶孔12,台阶孔12的上段是光孔,用来安装定位套,台阶孔12的下段是螺纹孔,用来固定连接用的螺栓;夹具体7的背面结构是:通过铣加工,设置有6个长方形的凹槽用于减重。Fig. 1, Fig. 2 are the upper and lower surface structure schematic diagrams of the clamp body 7 for processing the pulley frame side plate of the present invention, the clamp body 7 is made as a casting, the upper surface is the working surface, and symmetrical holes are arranged along the longitudinal axis both sides of the upper surface. The steps 13 and many holes 14 for positioning and installation are provided. A short through groove is arranged between the two steps 13. The bottom surface of the short through groove is a positioning surface 11 with high precision. A
参照图3、图4、图5,本发明的滑轮架侧板的加工定位方法,利用前述的装置,先将夹具体7固定在机床的工作台上,再将需要加工的滑轮架侧板6的光面放置在夹具体7短通槽的定位面11上,按照以下步骤实施:Referring to Fig. 3, Fig. 4, Fig. 5, the processing and positioning method of the pulley frame side plate of the present invention uses the aforementioned device to first fix the clamp body 7 on the workbench of the machine tool, and then place the pulley
第一步,采用多点定位进行粗加工,即用多个支撑钉8对滑轮架侧板6光面四个支撑面进行支撑定位,通过螺钉5将压板1压紧在台阶13上,通过辅助夹具A9和辅助夹具B10对滑轮架侧板6两端部位进行定位,各个压板1和辅助夹具的压紧端同时将滑轮架侧板6压紧在定位面11上,按照加工工艺实施粗加工;The first step is to use multi-point positioning for rough machining, that is, use
第二步,采用一点定位进行精加工,利用四个支撑钉8在滑轮架侧板6的四个角上分别进行辅助支撑,在滑轮架侧板6的装配孔中套入定位套4,将圆形压板3压在定位套4上端口,将螺栓2套进定位套4及定位面11的台阶孔12中,将滑轮架侧板6压紧在定位面11上,按照加工工艺实施精加工。In the second step, one-point positioning is used for finishing, and four supporting
滑轮架侧板左右件加工时分为粗加工和精加工两次,两次加工都在该工装上完成。粗加工时以侧板下边的四个圆台为定位支撑面,采用多点定位,压板压紧方式;精加工时为防止变形采用“一点定位”,侧边加销防转动。The processing of the left and right parts of the side plate of the pulley frame is divided into two times: rough machining and finishing machining, both of which are completed on the tooling. During rough machining, the four round tables under the side plate are used as the positioning support surface, and multi-point positioning is adopted, and the pressure plate is pressed; during finishing machining, "one point positioning" is adopted to prevent deformation, and pins are added on the side to prevent rotation.
利用本发明装置加工滑轮架侧板6时,将夹具体7固定的机床的工作台上,放置滑轮架侧板6,用压板1压紧滑轮架侧板6,粗加工滑轮架侧板6下边的四个圆台。松开压板1,滑轮架侧板6反转180度,以刚才加工好的四个圆台为定位面,铣切滑轮架侧板6上下厚度达到要求。精加工时,采用一点定位,将滑轮架侧板6放置在夹具体7上,并使滑轮架侧板6上指定的装配孔与夹具体上的定位套4配合,并用圆形压板3压在滑轮架侧板6上后,用螺母拧紧,使滑轮架侧板6夹紧在夹具体上;同时在滑轮架侧板6的四个角上用支撑钉8进行辅助。When utilizing the device of the present invention to process the pulley
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201110324180.5A CN102501101B (en) | 2011-10-24 | 2011-10-24 | Clamp body for machining side plate of pulley frame, and method for machining and positioning side plate of pulley frame |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201110324180.5A CN102501101B (en) | 2011-10-24 | 2011-10-24 | Clamp body for machining side plate of pulley frame, and method for machining and positioning side plate of pulley frame |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN102501101A true CN102501101A (en) | 2012-06-20 |
| CN102501101B CN102501101B (en) | 2014-04-09 |
Family
ID=46213266
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201110324180.5A Active CN102501101B (en) | 2011-10-24 | 2011-10-24 | Clamp body for machining side plate of pulley frame, and method for machining and positioning side plate of pulley frame |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102501101B (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102990449A (en) * | 2012-11-19 | 2013-03-27 | 无锡市航鹄科技有限公司 | Positioning device for high-efficiency linear cutting |
| CN103522221A (en) * | 2013-10-24 | 2014-01-22 | 随州润晶电子科技有限公司 | Device for bidirectionally positioning and clamping wafer |
| CN103639778A (en) * | 2013-11-29 | 2014-03-19 | 无锡市航鹄科技有限公司 | Positioning tool for milling |
| CN106272130A (en) * | 2016-10-11 | 2017-01-04 | 上海翼锐汽车科技有限公司 | Protecgulum flexible fixture |
Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN85109558A (en) * | 1984-12-10 | 1986-06-10 | 查尔斯·亚当斯 | precise positioning device |
| CN1100021A (en) * | 1993-05-04 | 1995-03-15 | 厄罗瓦公司 | An apparatus for clamping a work piece in a well defined position |
| JPH10328957A (en) * | 1997-03-27 | 1998-12-15 | Hitachi Ltd | Scroll shape processing device and processing method |
| JP2003048130A (en) * | 2001-08-03 | 2003-02-18 | Ykk Corp | Work fixing jig |
| CN2880363Y (en) * | 2006-02-13 | 2007-03-21 | 许晓华 | Porous deformed plate milling drilling clamp |
| WO2010126405A1 (en) * | 2009-04-29 | 2010-11-04 | Flexprop Ab | Holder and fixing plate therefor |
| CN201807913U (en) * | 2010-06-25 | 2011-04-27 | 昆山美和机械有限公司 | Clamp dedicated for machining |
| CN201871885U (en) * | 2010-11-25 | 2011-06-22 | 北京特种机械研究所 | Adjustable tensioning and supporting device |
| CN201940830U (en) * | 2010-12-21 | 2011-08-24 | 山东新安凯动力科技有限公司 | Fixture for automatic shifting transmission case shell |
-
2011
- 2011-10-24 CN CN201110324180.5A patent/CN102501101B/en active Active
Patent Citations (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN85109558A (en) * | 1984-12-10 | 1986-06-10 | 查尔斯·亚当斯 | precise positioning device |
| CN1100021A (en) * | 1993-05-04 | 1995-03-15 | 厄罗瓦公司 | An apparatus for clamping a work piece in a well defined position |
| JPH10328957A (en) * | 1997-03-27 | 1998-12-15 | Hitachi Ltd | Scroll shape processing device and processing method |
| JP2003048130A (en) * | 2001-08-03 | 2003-02-18 | Ykk Corp | Work fixing jig |
| CN2880363Y (en) * | 2006-02-13 | 2007-03-21 | 许晓华 | Porous deformed plate milling drilling clamp |
| WO2010126405A1 (en) * | 2009-04-29 | 2010-11-04 | Flexprop Ab | Holder and fixing plate therefor |
| CN201807913U (en) * | 2010-06-25 | 2011-04-27 | 昆山美和机械有限公司 | Clamp dedicated for machining |
| CN201871885U (en) * | 2010-11-25 | 2011-06-22 | 北京特种机械研究所 | Adjustable tensioning and supporting device |
| CN201940830U (en) * | 2010-12-21 | 2011-08-24 | 山东新安凯动力科技有限公司 | Fixture for automatic shifting transmission case shell |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102990449A (en) * | 2012-11-19 | 2013-03-27 | 无锡市航鹄科技有限公司 | Positioning device for high-efficiency linear cutting |
| CN103522221A (en) * | 2013-10-24 | 2014-01-22 | 随州润晶电子科技有限公司 | Device for bidirectionally positioning and clamping wafer |
| CN103639778A (en) * | 2013-11-29 | 2014-03-19 | 无锡市航鹄科技有限公司 | Positioning tool for milling |
| CN106272130A (en) * | 2016-10-11 | 2017-01-04 | 上海翼锐汽车科技有限公司 | Protecgulum flexible fixture |
Also Published As
| Publication number | Publication date |
|---|---|
| CN102501101B (en) | 2014-04-09 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN108772737B (en) | Bearing seat turning process and fixture thereof | |
| CN103949909A (en) | CNC (computer numerical control) machined spherical piece combined clamp and clamping method | |
| CN206662766U (en) | Aerial blade fixture | |
| CN209902719U (en) | A fixture for fixing square eccentric parts for lathes | |
| CN102501101B (en) | Clamp body for machining side plate of pulley frame, and method for machining and positioning side plate of pulley frame | |
| CN115570415A (en) | Special-shaped profile part machining tool and using method thereof | |
| CN202804743U (en) | Finish machining fixture for small end plane of engine connecting rod | |
| CN202356930U (en) | Processing fixture for hydraulic pump location hole | |
| CN102672491B (en) | Special clamp for micro-milling blank | |
| CN201279680Y (en) | Quickly clamping machine tool workbench | |
| CN216608067U (en) | Machining universal fixture | |
| CN110757202A (en) | Intensive automobile panel mould processing workstation | |
| CN215747917U (en) | Clamp for rapid key groove milling of numerical control machining center | |
| CN105500058B (en) | A kind of CNC processing bool special fixtures and clamping method | |
| CN214979379U (en) | Special-shaped tailstock eccentric hole turning clamp | |
| CN204893486U (en) | Quick clamping positioning fixture | |
| CN117381483A (en) | A processing device for curved wall panels and a method of using the same | |
| CN204524881U (en) | A kind of four-way class non-coaxial pressure inlet part fixture for processing | |
| CN204108665U (en) | The Work fixing device of four axle lathes | |
| CN202317761U (en) | Special fixture for turntable processing | |
| CN108356562B (en) | A jig for processing rivet holes of blade assemblies riveted with multi-layer thin-walled parts | |
| CN108007680B (en) | A special fixture for force measurement with low additional vibration for thin-walled plates | |
| CN223477004U (en) | Special frock of front axle taper hole processing | |
| CN202097568U (en) | Combined V-shaped block structure | |
| CN112847180B (en) | A tooling fixture for connecting plate of upper tube socket of fuel assembly |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant |