CN102500728B - Stackable double-face tie wire forming device - Google Patents
Stackable double-face tie wire forming device Download PDFInfo
- Publication number
- CN102500728B CN102500728B CN 201110354853 CN201110354853A CN102500728B CN 102500728 B CN102500728 B CN 102500728B CN 201110354853 CN201110354853 CN 201110354853 CN 201110354853 A CN201110354853 A CN 201110354853A CN 102500728 B CN102500728 B CN 102500728B
- Authority
- CN
- China
- Prior art keywords
- moving plate
- guide rail
- parts
- support frame
- production
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Wire Processing (AREA)
Abstract
一种可堆叠双面扣丝成型装置,属于扣丝生产设施技术领域,用于提高现有的自动扣丝机的稳定性、可调节功能和产能,其技术方案是:在设备的前后端增加了支撑框架,两条生产线平行固定安装在支撑框架内,每条生产线的静板和动板一侧的支撑框架之间安装有上下两条平行导轨,导轨位于支撑框架外侧,动板套装在导轨上,动板与导轨为可滑动配合,在动板上有导轨锁紧装置,在动板的另一侧外部安装有与导轨平行的动板支架,动板支架上安装有齿条,动板侧面安装有齿轮,齿轮和齿条相啮合,动板上安装有动板调节手柄,动板调节手柄与齿轮轴相连接。本发明具有结构合理、方便调整、生产线互不影响、稳定性好、可堆叠布设的优点,值得在同行业进行推广。
A stackable double-sided button thread forming device belongs to the technical field of button thread production facilities and is used to improve the stability, adjustable function and production capacity of the existing automatic button thread machine. The technical solution is: add Two production lines are fixed and installed in the support frame in parallel. Two parallel guide rails are installed between the static plate and the support frame on the side of the moving plate of each production line. The guide rails are located outside the support frame, and the moving plate is set on the guide rail. On the upper side, the moving plate and the guide rail are slidable, and there is a guide rail locking device on the moving plate, and a moving plate bracket parallel to the guide rail is installed on the other side of the moving plate, and a rack is installed on the moving plate bracket, and the moving plate A gear is installed on the side, and the gear and the rack are meshed. A moving plate adjusting handle is installed on the moving plate, and the moving plate adjusting handle is connected with the gear shaft. The invention has the advantages of reasonable structure, convenient adjustment, no mutual influence of production lines, good stability and stackable arrangement, and is worthy of popularization in the same industry.
Description
技术领域 technical field
本发明涉及一种加工扣丝的成型设施,属于扣丝生产设施技术领域。 The present invention relates to a forming facility for processing buckle threads, which belongs to the technical field of buckle thread production facilities.
背景技术 Background technique
扣丝是近年来开始用于搭建建筑混凝土构件钢筋骨架和垃圾袋等用的捆扎件,利用该件可方便快速地形成紧且不易松动的捆扎头,故得到建筑等行业的青睐,有广阔的市场前途。为了适应对扣丝的大批量需求,开发能够进行自动化生产的加工设备是非常必要的,中国专利号“ZL200610048245.7”公开了一种扣丝成型机,这种扣丝成型机在技术上解决了扣丝成型生产的自动化问题,但在生产化过程中有如下不足: The buckle wire is a binding piece that has been used in building concrete components, steel bars, and garbage bags in recent years. It can be used to quickly and easily form a tight and not easy to loose binding head, so it is favored by construction and other industries and has a broad market market prospects. In order to meet the large-scale demand for threading, it is very necessary to develop processing equipment capable of automatic production. It solves the automation problem of wire forming production, but has the following deficiencies in the production process:
1. 采用三条生产线并行方式,每条线生产不可单独控制,三线扭丝机构采用同一气缸驱动,要求传动机构的制造、装配精度高,调整难度大; 1. Three production lines are used in parallel, and the production of each line cannot be controlled separately. The three-line twisting mechanism is driven by the same cylinder, which requires high manufacturing and assembly precision of the transmission mechanism and is difficult to adjust;
2. 三条生产线采用上下平行布局,三线之间垂直距离短,成型后扣丝下料时相互易发生干涉缠结在一起; 2. The three production lines adopt an up-and-down parallel layout, and the vertical distance between the three lines is short, so they are prone to interference and entanglement when threading and blanking after forming;
3. 该设备为适应不同长度规格扣丝的加工,将两侧弯丝部件分别固定在静板和动板上,调整时要将动板整体滑动调整,调整要达到需要的精确度费时、费力; 3. In order to adapt to the processing of threading with different lengths and specifications, the equipment fixes the wire bending parts on both sides on the static plate and the moving plate respectively. When adjusting, the moving plate should be adjusted by sliding as a whole. It is time-consuming and labor-intensive to adjust to achieve the required accuracy. ;
4. 该设备的校直送丝机构只能在垂直方向上进行校直,因此仍有部分金属丝存在有弯头的现象,直接影响了进丝; 4. The straightening wire feeding mechanism of this equipment can only be straightened in the vertical direction, so there are still some bends in the metal wires, which directly affects the wire feeding;
5. 设备重心在设备前端面,稳定性差,在实际工作中占用工作空间大。 5. The center of gravity of the equipment is at the front end of the equipment, which has poor stability and occupies a large working space in actual work.
发明内容 Contents of the invention
本发明所要解决的技术问题是提供一种在原有扣丝成型机的基础上,能够克服原有扣丝成型机以上不足的结构合理、方便调整、生产线互不影响、稳定性好的可堆叠双面扣丝成型装置。 The technical problem to be solved by the present invention is to provide a stackable double-layer machine with reasonable structure, convenient adjustment, independent production lines and good stability on the basis of the original thread forming machine, which can overcome the above shortcomings of the original thread forming machine. Surface button thread forming device.
解决上述技术问题的技术方案是: The technical scheme that solves the above-mentioned technical problem is:
一种可堆叠双面扣丝成型装置,它包括两条扣丝弯折生产线,每条生产线中有左右弯丝部件、导丝板部件、驱动减速部件、左右垂直成型部件、左右水平成型部件、左右下压头部件、切断部件、送丝部件、垂直校直部件,其改进之处是:在设备的前后端增加了支撑框架,两条生产线平行固定安装在支撑框架内,两条生产线由一台电动机提供动力,组成一个生产单元;每条生产线的静板和动板一侧的支撑框架之间安装有上下两条平行导轨,导轨位于支撑框架外侧,动板套装在导轨上,动板与导轨为可滑动配合,在动板上有导轨锁紧装置,在动板的另一侧外部安装有与导轨平行的动板支架,动板支架上安装有齿条,动板侧面安装有齿轮,齿轮和齿条相啮合,动板上安装有动板调节手柄,动板调节手柄与齿轮轴相连接。 A stackable double-sided wire forming device, which includes two wire bending production lines, each production line has left and right wire bending parts, wire guide plate parts, drive deceleration parts, left and right vertical forming parts, left and right horizontal forming parts, The improvement of the left and right lower pressure head parts, cutting parts, wire feeding parts, and vertical alignment parts is: a supporting frame is added at the front and rear ends of the equipment, and the two production lines are fixed and installed in the supporting frame in parallel. The two production lines are composed of A motor provides power to form a production unit; two parallel guide rails are installed between the static plate and the support frame on the side of the moving plate in each production line. The guide rail is located outside the support frame, and the moving plate is set on the guide rail. It is slidably matched with the guide rail, and there is a guide rail locking device on the moving plate, and a moving plate bracket parallel to the guide rail is installed outside the other side of the moving plate. A rack is installed on the moving plate bracket, and a gear is installed on the side of the moving plate. , the gear and the rack are meshed, a moving plate adjustment handle is installed on the moving plate, and the moving plate adjusting handle is connected with the gear shaft.
上述可堆叠双面扣丝成型装置,所述每条生产线的垂直校直部件后部增加了水平校直部件。 In the aforementioned stackable double-sided button thread forming device, a horizontal straightening component is added to the rear of the vertical straightening component of each production line.
上述可堆叠双面扣丝成型装置,所述校直机构和折弯机构之间添加牵引轮,牵引轮位于金属丝的上下两侧,双面牵引轮均与电磁离合器相连接。 In the above-mentioned stackable double-sided button thread forming device, traction wheels are added between the straightening mechanism and the bending mechanism. The traction wheels are located on the upper and lower sides of the wire, and the double-sided traction wheels are connected with electromagnetic clutches.
上述可堆叠双面扣丝成型装置,所述切断机构位于成型机构之前,切断部件安装在金属丝下方。 In the aforementioned stackable double-sided button thread forming device, the cutting mechanism is located in front of the forming mechanism, and the cutting component is installed under the wire.
上述可堆叠双面扣丝成型装置,所述由前后支撑框架构成的生产单元有多个,它们上下重叠放置,上下支撑框架分别有定位凹槽和定位凸起,定位凹槽和定位凸起相互对应与匹配。 In the above-mentioned stackable double-sided button thread forming device, there are multiple production units composed of front and rear support frames, which are stacked up and down. The upper and lower support frames have positioning grooves and positioning protrusions respectively, and the positioning grooves and positioning protrusions are mutually Correspondence and matching.
本发明的有益之处在于: The benefits of the present invention are:
1. 在设备的前后端增加了支撑框架,两条生产线平行固定安装在支撑框架内,组成一个生产单元,大大增加了设备牢固性和稳定性; 1. A supporting frame is added at the front and rear ends of the equipment, and the two production lines are fixed and installed in the supporting frame in parallel to form a production unit, which greatly increases the firmness and stability of the equipment;
2. 动板套装在导轨上,通过转动动板上的动板调节手柄带动齿轮和调整齿条的相对运动,从而实现动板在动板导轨上滑动, 达到扣丝长度的精确可调; 2. The moving plate is set on the guide rail, and the relative movement of the gear and the adjustment rack is driven by turning the moving plate adjustment handle on the moving plate, so that the moving plate slides on the moving plate guide rail to achieve accurate adjustment of the thread length;
3.增加了水平校直部件,使金属丝的校直效果更好,避免了弯头金属丝对生产的影响; 3. The horizontal straightening parts are added to make the straightening effect of the metal wire better and avoid the influence of the elbow metal wire on the production;
4.采用堆叠式结构可以大大节约了占地面积,显著提高生产率和经济效益。 4. The use of a stacked structure can greatly save the floor space and significantly improve productivity and economic benefits.
本发明通过以上改进,取得了非常显著的效果,使扣丝生产的质量和数量都得到了大大提高,对满足市场的需求做出了很大贡献,值得在同行业进行推广。 Through the above improvements, the present invention has achieved very remarkable effects, greatly improving the quality and quantity of button thread production, making a great contribution to meeting the market demand, and worthy of promotion in the same industry.
附图说明 Description of drawings
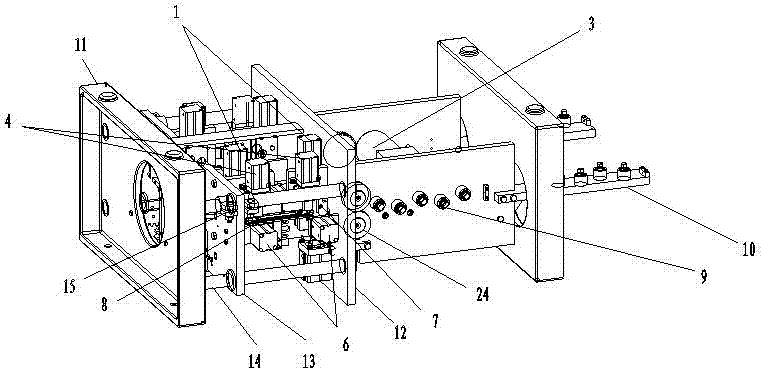
图1是本发明的结构示意图; Fig. 1 is a structural representation of the present invention;
图2是本发明的主视图; Fig. 2 is the front view of the present invention;
图3是本发明的俯视图; Fig. 3 is a top view of the present invention;
图4是本发明的仰视图 Fig. 4 is the bottom view of the present invention
图5是本发明的堆叠状态图。 Fig. 5 is a stacked state diagram of the present invention.
图中标记如下:左右弯丝部件1、导丝板部件2、驱动减速部件3、左右垂直成型部件4、左右水平成型部件5、左右下压头部件6、切断部件7、送丝部件8、垂直校直部件9、水平校直部件10、支撑框架11、静板12、动板13、导轨14、导轨锁紧装置15、动板支架16、齿条17、齿轮18、动板调节手柄19、导丝平推气缸20、下压导块21、下压板22、电磁离合器23、送丝主动轮24。
The markings in the figure are as follows: left and right
具体实施方式 Detailed ways
本发明为了提高生产效率,采用堆叠双面扣丝成型装置,分两条生产线保证可同时工作,同时也可单独工作,生产效率高。为了减少扣丝成型装置工作时所占空间,采用多台成型机可堆叠结构,支撑框架上设置定位槽保证扣丝机工作的稳定性,且上下两台设备之间距离保证扣丝成型后下料不发生干涉。 In order to improve production efficiency, the present invention adopts a stacked double-sided button thread forming device, which is divided into two production lines to ensure that they can work at the same time, and can also work independently at the same time, and the production efficiency is high. In order to reduce the space occupied by the threading forming device when it is working, a stackable structure of multiple forming machines is adopted. Positioning grooves are set on the supporting frame to ensure the stability of the threading machine, and the distance between the upper and lower devices ensures that the threading machine is lowered after forming. Material does not interfere.
本发明的每条生产线中有左右弯丝部件1、导丝板部件2、驱动减速部件3、左右垂直成型部件4、左右水平成型部件5、左右下压头部件6、切断部件7、送丝部件8、垂直校直部件9、水平校直部件10、支撑框架11。
In each production line of the present invention, there are left and right
图中显示,两条生产线平行固定安装在支撑框架11内,两条生产线由一台电动机提供动力,组成一个生产单元。
As shown in the figure, two production lines are fixedly installed in the
图中显示,每条生产线的静板12和动板13一侧的支撑框架11之间安装有上下两条平行导轨14,导轨14位于支撑框架11外侧,动板13套装在导轨14上,动板13可以沿着导轨14滑动,在动板13上有导轨锁紧装置15。在动板13的另一侧外部安装有与导轨14平行的动板支架16,动板支架16可以防止导轨14受到扭矩。动板支架16上安装有齿条17,动板13侧面安装有齿轮18,齿轮18和齿条17相啮合,动板13上安装有动板调节手柄19,动板调节手柄19与齿轮轴相连接。通过转动动板13上的动板调节手柄19带动齿轮18和调整齿条17的相对运动,从而实现动板13在动板导轨14上滑动,到位后锁紧导轨锁紧装置15,最终实现扣丝的长度可调。
As shown in the figure, two upper and lower
图中显示,在送丝端安装水平校直部件10和垂直校直部件9,分别对金属丝的竖直和水平方向进行校直。
As shown in the figure, a
金属丝经校直后需要进行折弯和切断,在加工之前需要实现金属丝的送丝动作,因此需要在校直机构和折弯机构之间添加牵引机构。因为要实现双面独立工作,所以双面牵引轮均与电磁离合器23相连接,可以让电机不停转,通过PLC控制电磁离合器23的连接与断开来控制送丝主动轮24的停、转。
The metal wire needs to be bent and cut after being straightened, and the wire feeding action of the metal wire needs to be realized before processing, so a traction mechanism needs to be added between the straightening mechanism and the bending mechanism. Because the double-sided independent work is to be realized, the double-sided traction wheels are all connected with the electromagnetic clutch 23, so that the motor can not stop running, and the connection and disconnection of the electromagnetic clutch 23 can be controlled by PLC to control the stop and turn of the wire
在进行折弯时,还应对金属丝进行切断。在金属丝送丝到位后,金属丝需要进行定长切断,因此切断部件7安装在成型机构之前,为了不使机构之间发生干涉,需要将金属丝从下面开始切断,防止成型气缸和切断气缸之间产生干涉现象。 When bending, the wire should also be cut. After the wire is fed in place, the wire needs to be cut at a fixed length, so the cutting part 7 is installed before the forming mechanism. In order not to interfere with the mechanism, the wire needs to be cut from the bottom to prevent the forming cylinder and the cutting cylinder from forming. interference between them.
图中显示,为了给生产单位节省更多的空间,可以将扣丝机设计为堆叠式,扣丝机的支撑框架11设计为强度很高的槽型结构,在支撑框架11的上面有定位凸起,下面有定位凹槽,在堆叠放置时只需让上面扣丝机的定位凹槽对准下面扣丝机的定位凸起放置即可。
As shown in the figure, in order to save more space for the production unit, the threading machine can be designed as stacked, and the supporting
Claims (3)
- One kind can stacking double sided button silk shaped device, it comprises two button silk bending production lines, the left and right sides curved silk parts (1) are arranged in every production line, thread plate parts (2), drive deceleration component (3), left and right sides vertical forming parts (4), left and right horizontal profiled part (5), left and right sides push-down head parts (6), cut off parts (7), wire feed parts (8), vertical alignment parts (9), it is characterized in that: increased support frame (11) in the front and back end of equipment, article two, production line is parallel is fixedly mounted in the support frame (11), article two, production line provides power by a motor, forms a production unit; Up and down two closed slides (14) are installed between the quiet plate (12) of every production line and the support frame (11) of moving plate (13) one sides, guide rail (14) is positioned at support frame (11) outside, moving plate (13) is sleeved on the guide rail (14), moving plate (13) and guide rail (14) are for slidably cooperating, at moving plate (13) guide rail locking apparatus (15) is arranged, opposite side outside at moving plate (13) is equipped with the moving board mount (16) parallel with guide rail (14), on the moving board mount (16) tooth bar (17) is installed, moving plate (13) side is equipped with gear (18), gear (18) and tooth bar (17) are meshed, moving plate regulating handle (19) is installed on the moving plate (13), and moving plate regulating handle (19) is connected with gear shaft.
- 2. according to claim 1 can stacking double sided button silk shaped device, it is characterized in that: vertical alignment parts (9) rear portion of described every production line has increased horizontal alignment parts (10).
- 3. according to claim 1 and 2 can stacking double sided button silk shaped device, it is characterized in that: the described production unit that is made of front and back support frame (11) has a plurality of, their up and down overlapping placements, support frame (11) has respectively detent and positioning convex up and down, and detent and positioning convex be corresponding and coupling mutually.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201110354853 CN102500728B (en) | 2011-11-10 | 2011-11-10 | Stackable double-face tie wire forming device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201110354853 CN102500728B (en) | 2011-11-10 | 2011-11-10 | Stackable double-face tie wire forming device |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN102500728A CN102500728A (en) | 2012-06-20 |
| CN102500728B true CN102500728B (en) | 2013-10-30 |
Family
ID=46212894
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201110354853 Expired - Fee Related CN102500728B (en) | 2011-11-10 | 2011-11-10 | Stackable double-face tie wire forming device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102500728B (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105344778A (en) * | 2015-11-27 | 2016-02-24 | 蒋中意 | Stainless steel corner line cold bending forming machine |
| CN110984480B (en) * | 2019-12-23 | 2021-08-20 | 浙江捷城建筑科技有限公司 | A prefabricated column main rib positioning and fixing device |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3623514A (en) * | 1969-12-30 | 1971-11-30 | Sickinger Co Hans | Machine for the manufacture of wire binders |
| CN2701068Y (en) * | 2004-01-13 | 2005-05-18 | 镇江金盛机械有限公司 | Hooking mechanism for threading machine |
| CN1915555A (en) * | 2006-09-06 | 2007-02-21 | 河北科技大学 | Forming machine for screw thread |
| US7523633B1 (en) * | 2005-10-27 | 2009-04-28 | Mielke Laurence H | Wire tray jig and bending method |
-
2011
- 2011-11-10 CN CN 201110354853 patent/CN102500728B/en not_active Expired - Fee Related
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3623514A (en) * | 1969-12-30 | 1971-11-30 | Sickinger Co Hans | Machine for the manufacture of wire binders |
| CN2701068Y (en) * | 2004-01-13 | 2005-05-18 | 镇江金盛机械有限公司 | Hooking mechanism for threading machine |
| US7523633B1 (en) * | 2005-10-27 | 2009-04-28 | Mielke Laurence H | Wire tray jig and bending method |
| CN1915555A (en) * | 2006-09-06 | 2007-02-21 | 河北科技大学 | Forming machine for screw thread |
Also Published As
| Publication number | Publication date |
|---|---|
| CN102500728A (en) | 2012-06-20 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN203612601U (en) | Elevator door board conveying location device | |
| CN202336516U (en) | Platform pipe bender | |
| CN202639056U (en) | Intelligent guide rail forming machine | |
| CN102500728A (en) | Stackable double-face tie wire forming device | |
| CN102198726B (en) | Drinking straw corrugating device | |
| CN201552335U (en) | Production line for transversely cutting two parallel coil materials | |
| CN203281682U (en) | Co-moving type cold roll forming device | |
| CN202052802U (en) | Nine-roller flattener | |
| CN206098138U (en) | Z style of calligraphy inductance coils integrated into one piece equipment | |
| CN206898129U (en) | A kind of high-precision automatic roll bending equipment | |
| CN204685787U (en) | T-shaped keel automatic punching die cutting machine | |
| CN104400825A (en) | Curing, cutting and molding integrated machine for polyester fiber material | |
| CN213223853U (en) | Pipe making machine for hot-dip galvanized steel strip processing | |
| CN204381116U (en) | The fin levelling device of multistep formation type fin rolling belt machine | |
| CN202824673U (en) | Lead screw drive slider | |
| CN202045865U (en) | Beverage sucker corrugation pressing equipment | |
| CN202744600U (en) | A large multifunctional roll quenching machine tool | |
| CN210334143U (en) | Automatic wire feeding and cutting mechanism for wire rod pretreatment | |
| CN205004176U (en) | Be applied to forming device of ribbon line coiling machine | |
| CN201446719U (en) | Profiling plate machine | |
| CN207790133U (en) | A kind of plank embossing machine | |
| CN206296663U (en) | Bender | |
| CN206591188U (en) | A kind of linear electro-deposition large size copper steel clad wire production equipment | |
| CN207682382U (en) | A kind of Die-casting Machines hand both arms handle composite assemble mechanism | |
| CN205764503U (en) | A kind of effective integrated self-feeding welding mechanism |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20131030 Termination date: 20141110 |
|
| EXPY | Termination of patent right or utility model |