WO2025005169A1 - 冷延鋼板 - Google Patents
冷延鋼板 Download PDFInfo
- Publication number
- WO2025005169A1 WO2025005169A1 PCT/JP2024/023290 JP2024023290W WO2025005169A1 WO 2025005169 A1 WO2025005169 A1 WO 2025005169A1 JP 2024023290 W JP2024023290 W JP 2024023290W WO 2025005169 A1 WO2025005169 A1 WO 2025005169A1
- Authority
- WO
- WIPO (PCT)
- Prior art keywords
- steel sheet
- goss
- grains
- grain
- oriented
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Ceased
Links
Images

Classifications
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/16—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys in the form of sheets
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1216—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the working steps
- C21D8/1233—Cold rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1244—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment
- C21D8/1255—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment with diffusion of elements, e.g. decarburising, nitriding
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1244—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment
- C21D8/1261—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment following hot rolling
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1244—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties characterised by the heat treatment
- C21D8/1272—Final recrystallisation annealing
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
- C21D8/12—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties
- C21D8/1294—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment during manufacturing of articles with special electromagnetic properties involving a localised treatment
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D9/00—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor
- C21D9/46—Heat treatment, e.g. annealing, hardening, quenching or tempering, adapted for particular articles; Furnaces therefor for sheet metals
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/002—Ferrous alloys, e.g. steel alloys containing In, Mg, or other elements not provided for in one single group C22C38/001 - C22C38/60
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/008—Ferrous alloys, e.g. steel alloys containing tin
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/14—Ferrous alloys, e.g. steel alloys containing titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/16—Ferrous alloys, e.g. steel alloys containing copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/20—Ferrous alloys, e.g. steel alloys containing chromium with copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/26—Ferrous alloys, e.g. steel alloys containing chromium with niobium or tantalum
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/34—Ferrous alloys, e.g. steel alloys containing chromium with more than 1.5% by weight of silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/42—Ferrous alloys, e.g. steel alloys containing chromium with nickel with copper
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/46—Ferrous alloys, e.g. steel alloys containing chromium with nickel with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/48—Ferrous alloys, e.g. steel alloys containing chromium with nickel with niobium or tantalum
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/50—Ferrous alloys, e.g. steel alloys containing chromium with nickel with titanium or zirconium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/60—Ferrous alloys, e.g. steel alloys containing lead, selenium, tellurium, or antimony, or more than 0.04% by weight of sulfur
-
- H—ELECTRICITY
- H01—ELECTRIC ELEMENTS
- H01F—MAGNETS; INDUCTANCES; TRANSFORMERS; SELECTION OF MATERIALS FOR THEIR MAGNETIC PROPERTIES
- H01F1/00—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties
- H01F1/01—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials
- H01F1/03—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity
- H01F1/12—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials
- H01F1/14—Magnets or magnetic bodies characterised by the magnetic materials therefor; Selection of materials for their magnetic properties of inorganic materials characterised by their coercivity of soft-magnetic materials metals or alloys
- H01F1/147—Alloys characterised by their composition
- H01F1/14766—Fe-Si based alloys
- H01F1/14775—Fe-Si based alloys in the form of sheets
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D2201/00—Treatment for obtaining particular effects
- C21D2201/05—Grain orientation
Definitions
- the present invention relates to a cold-rolled steel sheet for use in a grain-oriented electrical steel sheet.
- Grain-oriented electrical steel sheet contains silicon, and the crystal orientation of its crystal grains is concentrated near the Goss orientation (cubic ⁇ 110 ⁇ 001>), with the ⁇ 001> orientation, which is the axis of easy magnetization, being nearly aligned with the rolling direction in the steel sheet manufacturing process.
- Such grain-oriented electrical steel sheet is extremely useful as a material for the iron cores of transformers, etc.
- the most important are magnetic flux density and core loss.
- Magnetic flux density B8 is generally used as an index of magnetic flux density.
- Magnetic flux density B8 is the value of the magnetic flux density of a magnetized grain-oriented electrical steel sheet when a magnetizing force of 800 A/m is applied in the rolling direction.
- a grain-oriented electrical steel sheet with a higher magnetic flux density B8 value is more easily magnetized with a certain magnetizing force and has a higher magnetic flux density, making it suitable for small, highly efficient transformers.
- the iron loss W17/ 50 is generally used as an index of iron loss.
- the iron loss W17 /50 is the iron loss when a grain-oriented electrical steel sheet is excited with an AC current under conditions of a maximum magnetic flux density of 1.7 T and a frequency of 50 Hz. It can be said that the smaller the value of the iron loss W17/ 50 of a grain-oriented electrical steel sheet, the lower the energy loss and the more suitable it is for a transformer.
- the magnetic domain control method using grooves has a problem of a decrease in magnetic flux density B 8 .
- grain-oriented electrical steel sheets are manufactured as follows.
- a steel sheet material (slab) containing a specified amount of Si is hot-rolled, annealed, and cold-rolled to obtain a steel sheet of the desired thickness.
- the cold-rolled steel sheet is then annealed (also called primary annealing or decarburization annealing).
- This annealing causes primary recrystallization, and within the primary recrystallized grains, crystal grains are formed that have a crystal orientation with an angle of deviation of 10° or less from the strict Goss orientation described by ⁇ 110 ⁇ 001>, with the axis of easy magnetization aligned in the rolling direction (hereinafter referred to as Goss orientation grains).
- This annealing also serves as decarburization annealing.
- an annealing separator mainly composed of MgO is applied to the surface of the steel sheet where primary recrystallization has occurred.
- the steel sheet coated with the annealing separator is wound up to produce a steel sheet coil, and this steel sheet coil is subjected to batch annealing (also called secondary recrystallization annealing or finish annealing).
- This annealing causes the Goss orientation grains to eat away at other crystal grains, causing secondary recrystallization and forming a so-called glass coating on the surface of the steel sheet.
- the Goss orientation grains grow preferentially due to the influence of inhibitors contained in the steel sheet, and the grain size of larger grains may be 100 mm or more.
- annealing is performed to flatten the steel sheet where secondary recrystallization has occurred, and an insulating coating is formed, etc.
- grain-oriented electrical steel sheets obtain predetermined magnetic properties by inducing secondary recrystallization during final annealing to obtain a crystal structure consisting of Goss-oriented grains accumulated in the ⁇ 110 ⁇ 001> orientation.
- it is effective to increase the frequency of minor Goss-oriented grains and to increase the frequency of grains that have good crystal lattice matching with the Goss-oriented grains after primary annealing.
- crystal grains of ⁇ 778 ⁇ 447>( ⁇ 111 ⁇ 112>) orientation and ⁇ 411 ⁇ 148> orientation are crystal grains that are easily encroached upon by the Goss-oriented grains, and it is effective to include a large number of them in the primary recrystallized structure.
- corresponding orientation grains crystal grains of ⁇ 778 ⁇ 447>( ⁇ 111 ⁇ 112>) orientation and ⁇ 411 ⁇ 148> orientation
- the frequency of the corresponding orientation grains that are easily encroached by the Goss orientation grains increases with an increase in the cold rolling reduction
- the frequency of the Goss orientation grains decreases with an increase in the cold rolling reduction.
- the frequency of the Goss orientation grains, which are the minor orientation in the primary recrystallization texture increases as the heating rate of the primary annealing increases
- the frequency of the corresponding orientation grains, which have the ⁇ 111 ⁇ 112> orientation which is the major orientation in the primary recrystallization texture, decreases as the heating rate of the primary annealing increases. That is, under conventional process control conditions, it has not been possible to independently control the frequency of existence of Goss-oriented grains and the frequency of existence of grains of a corresponding orientation that are easily encroached upon by the Goss-oriented grains.
- deviation angle ⁇ the deviation angle of the crystal orientation observed in the grain-oriented electrical steel sheet from the ideal ⁇ 110 ⁇ 001> orientation around the normal direction Z (ND) of the rolling surface
- deviation angle ⁇ the deviation angle from the ideal ⁇ 110 ⁇ 001> orientation around the direction perpendicular to the rolling direction C (TD)
- deviation angle ⁇ the deviation angle from the ideal ⁇ 110 ⁇ 001> orientation around the rolling direction L (RD)
- deviation angle ⁇ the deviation angle ⁇ .
- the Goss-oriented grains are not crystal grains (called ideal Goss-oriented grains) that have a Goss orientation (ideal Goss orientation) in the strict sense.
- the magnetization easy axis direction (cubic ⁇ 110 ⁇ 001>) of each crystal grain does not necessarily coincide completely with the rolling direction, and an angle deviation ⁇ exists between the magnetization easy axis direction and the rolling direction.
- Crystal grains whose angle deviation ⁇ from the ideal Goss orientation based on (Equation 1) is 10° or less are called Goss-oriented grains (practical Goss-oriented grains).
- the angle deviation ⁇ of the practical Goss-oriented grains increases, the orientation of the crystal orientation decreases, and the magnetic flux density B8 decreases.
- the Goss-oriented grains contained in steel sheets after primary recrystallization also contain grains with a large angle deviation ⁇ .
- the smaller the angle deviation ⁇ among the Goss-oriented grains the greater the driving force for grain growth and the more likely they are to continue growing preferentially until secondary recrystallization is complete. Therefore, the smaller the angle deviation ⁇ of Goss-oriented grains, the more likely they are to have a larger grain size after secondary recrystallization.
- certain grains are preferentially grown, which inevitably makes it easier for the grain size to increase.
- the steel sheet is not flat but curved as it is wound into a coil, but the crystal grains grow while maintaining the linearity of the crystal orientation. Therefore, when the coiled steel sheet is unwound and flattened after secondary recrystallization, there are parts within the crystal grains where the direction of the easy axis of magnetization is not parallel to the surface of the grain-oriented electrical steel sheet.
- This coil unwinding mainly increases the value of the deviation angle ⁇ and also increases the angle deviation ⁇ .
- the increase in angle deviation ⁇ due to coil unwinding is more noticeable the larger the crystal grain size. In other words, Goss-oriented grains with a small angle deviation ⁇ tend to grow preferentially during secondary recrystallization, but if the secondary recrystallized grain size becomes coarse, the angle deviation ⁇ increases due to coil unwinding.
- Patent Document 1 discloses a technique in which an etching process is performed on the surface of a steel sheet after final cold rolling to form linear grooves that satisfy certain conditions, and then in the primary annealing, the heating rate in the steel sheet temperature range of 500°C to 750°C is made faster in the linear groove parts compared to parts other than the linear grooves.
- Patent Document 1 by artificially creating parts with fast and slow heating rates, parts with a high heating rate (linear groove parts) and parts with a high heating rate (parts other than the linear grooves) are arranged, where the frequency of (110)[001] oriented grains is actively increased.
- Patent Document 2 discloses a technique in which a laser beam is irradiated multiple times at a specified interval PL in the rolling direction toward the surface of a silicon steel sheet between cold rolling and finish annealing.
- the positions along the trajectory of the laser beam become grain boundaries that penetrate the front and back of the silicon steel sheet.
- the length of the crystal grains in the rolling direction is at most about 30 mm, which corresponds to the irradiation interval PL, and the angular deviation between the magnetization easy axis direction (cubic ⁇ 110 ⁇ 001>) and the rolling direction is within the range of 0° to 6°.
- Patent Document 3 discloses a method for manufacturing grain-oriented electrical steel sheet that is based on a high-temperature slab heating process, has a small difference in the degree of orientation concentration in the Goss orientation at the inner and outer periphery of a coil with different curvatures, and has a high magnetic flux density.
- linear local heating is performed on a cold-rolled steel sheet, and this linear heating portion acts as a barrier to the growth of secondary recrystallized grains, suppressing the growth of secondary recrystallized grains.
- the present invention has been made in consideration of the above problems.
- the object of the present invention is to provide a cold-rolled steel sheet for grain-oriented electrical steel sheet that can increase the magnetic flux density.
- the object of the present invention is to provide a cold-rolled steel sheet for grain-oriented electrical steel sheet that can increase the magnetic flux density while suppressing the coarsening of secondary recrystallized grain sizes.
- the gist of the present invention is as follows:
- a cold-rolled steel sheet for grain-oriented electrical steel sheet comprises:
- the deviation angle from the ideal Goss orientation with the normal direction of the rolling surface as the rotation axis is defined as ⁇
- the deviation angle from the ideal Goss orientation with the direction perpendicular to the rolling as the rotation axis is defined as ⁇ .
- the deviation angle of the crystal orientation measured at the measurement point on the plate surface is represented as ( ⁇ ⁇ ),
- a crystal grain having an angle deviation ⁇ of 10° or less is defined as a Goss oriented grain,
- a 100 mm x 100 mm area on the plate surface is defined as a divided section.
- the divided sections containing at least one Goss oriented grain having a grain size of 5 ⁇ m or more account for 30% or more by area of all the divided sections.
- a cold-rolled steel sheet for grain-oriented electrical steel sheet that can increase the magnetic flux density.
- a cold-rolled steel sheet for grain-oriented electrical steel sheet that can increase the magnetic flux density while suppressing the coarsening of secondary recrystallized grains.
- the magnetic flux density of the oriented electrical steel sheet can be increased. Furthermore, by suitably distributing the areas where localized rapid heating is performed within the cold-rolled steel sheet, the magnetic flux density can be increased while suppressing the coarsening of the secondary recrystallized grain size of the oriented electrical steel sheet.
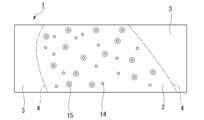
- FIG. 2 is a diagram showing an example of spot current heating used as a local rapid heating method, and is a schematic diagram showing an example of the arrangement of local heating regions in a cold-rolled steel sheet for a grain-oriented electrical steel sheet according to the present embodiment.
- FIG. 2 is a schematic diagram showing the distribution of Goss-oriented grains in a cold-rolled steel sheet for grain-oriented electrical steel sheet according to one embodiment of the present invention.
- Patent Document 1 forms linear grooves on the surface of a steel sheet by etching, and increases the heating rate of the linear grooves during primary annealing to arrange a portion with a high ratio of Goss orientation grains (linear groove portion) and a portion with a high ratio of corresponding orientation grains (portion other than the linear grooves).
- this method it is difficult to increase the difference in heating rate during primary annealing between the linear groove portion and other portions, and the effect obtained is limited. Specifically, the difference in heating rate between the linear groove portion and the portion other than the linear grooves is not so large.
- the degree to which the sheet thickness of this portion is thinned by the formation of the grooves does not exceed about 10% of the original sheet thickness (because the normal groove depth is about 20 ⁇ m or less, which is about 10% or less of the sheet thickness), and considering the thermal conductivity of the steel sheet, the heating rate ratio is less than the sheet thickness ratio for the same heat input, so the ratio of Goss orientation grains in the linear groove portion is difficult to increase compared to the portion other than the linear grooves.
- this method increases the heating rate of the linear groove portion during the primary annealing, so the grain size of the Goss-oriented grains formed in the linear groove portion after the primary annealing does not increase in size compared to the overall average primary recrystallized grain size, but remains the same or finer.
- Patent Document 2 irradiates a laser beam toward the steel sheet surface before finish annealing.
- the laser beam irradiation area is only controlled to the grain boundaries of secondary recrystallization, and the orientation of the Goss orientation grains generated by primary recrystallization is not controlled.
- the area heated by laser irradiation is only the area near the surface where the laser is irradiated, and there is significant thermal diffusion to the surrounding areas, so it is usually not possible to ensure a thermal history that will recrystallize the steel sheet.
- Patent Document 3 irradiates a laser beam toward the surface of the steel sheet after cold rolling.
- the laser beam irradiation portion is only controlled to the grain boundary of secondary recrystallization, and the heating rate is not controlled, so the orientation of the Goss orientation grains generated by primary recrystallization is not controlled.
- the laser beam irradiation portion acts as a barrier to the growth of secondary recrystallized grains, thereby only reducing the grain size in the rolling direction of the secondary recrystallized grains, and a grain growth temperature range in the local heating region that is effective for increasing the diameter of Goss orientation grains in the local heating region is not secured.
- This method may be able to reduce the difference in the degree of orientation accumulation in the Goss orientation at the inner and outer periphery of the coil with different curvatures, but it does not obtain Goss orientation grains whose crystal orientation is close to the ideal Goss orientation. In other words, this method suppresses the decrease in magnetic flux density due to the increase in the grain size in the rolling direction of secondary recrystallized grains, but does not aim to fundamentally improve the orientation of the Goss orientation grains.
- a grain-oriented electrical steel sheet with excellent quality can be obtained by locally and rapidly heating the steel sheet prior to the primary annealing (decarburization annealing) to form a locally heated region.
- the locally heated region formed prior to the primary annealing is arranged locally on the surface of the steel sheet.
- the crystalline structure of this locally heated region consists of one or both of a recrystallized structure and a recovered structure at the end of the localized rapid heating.
- the crystalline structure of the non-locally heated region of the steel sheet surface other than the locally heated region remains as it is cold-rolled and therefore consists of a cold-worked structure.
- the above-mentioned localized heating region preferably has a heating rate of 500°C/sec or more, preferably 2000°C/sec or more, more preferably 5000°C/sec or more, and even more preferably 10000°C/sec or more.
- a localized heating region is formed on the surface of a steel sheet before primary annealing, crystal grains having a practical Goss orientation are formed in the localized heating region.
- the proportion of Goss-oriented grains with smaller angular deviations ⁇ and ⁇ from the ideal Goss orientation increases, and the grain size of the Goss-oriented grains increases.
- the frequency of Goss-oriented grains in locally heated regions is greater than the frequency of Goss-oriented grains in non-locally heated regions. This characteristic is due to the fact that the non-locally heated regions retain the processed structure. Specifically, when local rapid heating is performed, recovery and recrystallization occur in the locally heated regions, resulting in the formation of practical Goss-oriented grains and facilitating grain growth, but recovery and recrystallization do not occur in non-locally heated regions.
- Goss-oriented grains formed in the locally heated areas grow preferentially during the secondary annealing after the primary annealing.
- Goss-oriented grains are formed in the locally heated areas, and among these grains are Goss-oriented grains with large crystal grain size that are close to the ideal Goss orientation with particularly small angle deviations ⁇ and ⁇ , and these Goss-oriented grains grow preferentially during the secondary recrystallization.
- the Goss orientation grains that serve as the nuclei for secondary recrystallization are supplied to the locally heated region, there is no need to form Goss orientation grains in the primary annealing in the matrix parts other than the locally heated region, i.e., the non-locally heated region other than the locally heated region. Therefore, as the heat treatment conditions for the primary annealing, a slow heating condition with a low heating rate may be adopted, and primary annealing conditions may be adopted that form many corresponding orientation grains with the easily eroded ⁇ 111 ⁇ 112> and ⁇ 411 ⁇ 148> orientations in the non-locally heated region.
- the heating rate for the primary annealing to 300°C/sec or less, many Goss orientation grains with large crystal grain size and close to the ideal Goss orientation are formed in the locally heated region, while almost no Goss orientation grains are formed in the non-locally heated region, and conversely, many corresponding orientation grains can be formed.
- spot current heating by electrical resistance heating
- spot electrodes are pressed against both sides of a steel sheet facing each other, and current is passed between the spot electrodes to spot current heating the electrode holding portion of the steel sheet.
- a steel having the composition shown in Table 1 was used, and a cold-rolled steel sheet with a sheet thickness of 0.22 mm was obtained by hot rolling and cold rolling. This steel sheet was subjected to spot current heating.
- the spot current heating was performed using a copper electrode with a diameter of 3 mm ⁇ , under the following conditions: the current was 5.0 kA or less, which is a range in which the steel sheet surface does not melt, the current time was 20 ms to 80 ms, the electrode pressure was 50 kgf to 150 kgf, and the electrode holding time after current was 0.2 seconds.
- Spot current heating was performed on the surface of the cold-rolled steel sheet in a grid pattern with a pitch of 30 mm in the rolling direction and a pitch of 30 mm in the width direction (perpendicular to the rolling direction), forming a localized heating area.
- Figure 1 shows an example of the arrangement of localized heating regions in a cold-rolled steel sheet for grain-oriented electrical steel sheet according to this embodiment.
- a steel sheet 1 localized heating regions 2, rolling direction 21, and width direction (direction perpendicular to rolling) 22 are shown diagrammatically.
- FIG. 1 is a schematic diagram showing the distribution of Goss orientation grains in the cold-rolled steel sheet for grain-oriented electrical steel sheet according to this embodiment.
- Figure 2 shows an observation area including a locally heated region 2 and a non-locally heated region (matrix portion) 3.
- the non-locally heated region 3 is a cold-worked structure. Therefore, when the IQ value is measured by EBSD after the above-mentioned pretreatment of the steel plate surface, the non-locally heated region 3 exhibits an IQ value of a cold-worked structure.
- the locally heated region 2 is a recovered structure and a recrystallized structure, so its IQ value is higher than that of a cold-worked structure.
- the locally heated region 2 and the non-locally heated region 3 can be identified, and the boundary between the locally heated region 2 and the non-locally heated region 3 (locally heated region boundary 4) can be confirmed. Note that when it is not easy to distinguish the local heated region boundary 4 by microstructural observation, the region containing Goss-oriented grains with a grain size of 5 ⁇ m or more can be regarded as the locally heated region 2.
- the current-carrying electrode used for spot current heating is circular, and its diameter is preferably 0.5 mm ⁇ to 10 mm ⁇ , and more preferably 1 mm ⁇ to 5 mm ⁇ , in terms of circle equivalent diameter. Note that, although a circular current-carrying electrode was used in the above, it is sufficient to locally increase the heating rate of the cold-rolled steel sheet, form Goss-oriented grains in this region, and allow the grains to grow; the electrode shape may be other shapes, for example, elliptical or linear.
- the cold-rolled steel sheet (steel sheet 1) for grain-oriented electrical steel sheet according to this embodiment contains Goss-oriented grains 14 and also contains coarse Goss-oriented grains 15.
- the region containing the coarse Goss-oriented grains 15 corresponds to the locally heated region 2. Note that almost no Goss-oriented grains are observed in the matrix portion 3 (non-locally heated region 3) where no local heating has been performed.
- the above cold-rolled steel sheet was used for primary annealing (decarburization annealing).
- primary annealing the cold-rolled steel sheet was heated at a heating rate of 100°C/sec and held at 830°C for 90 seconds.
- decarburization annealed steel sheet after the primary annealing many Goss-oriented grains were present in the locally heated areas, and these crystal grains had also grown. On the other hand, almost no Goss-oriented grains were observed in the matrix portion (non-locally heated area).
- the above decarburized annealed steel sheet was further subjected to nitriding treatment, and then an annealing separator mainly composed of MgO was applied, followed by secondary annealing.
- the secondary annealing conditions were a hydrogen-nitrogen atmosphere, a heating rate of 15°C/hour, and retention at 1200°C for 20 hours.
- the obtained steel sheet was subjected to macro-etching to reveal the grain boundaries. When the steel sheet after macro-etching was observed at a location corresponding to the local heating region, it was observed that a plurality of secondary recrystallized grains had grown from the location corresponding to the local heating region, and that secondary recrystallized grains had spread from the center of the location corresponding to the local heating region.
- the cold-rolled steel sheet according to this embodiment contains Goss orientation grains 14 as well as coarse Goss orientation grains 15. It is believed that the formation of coarse Goss orientation grains 15 close to the ideal Goss orientation with a size advantage is the cause of the good secondary recrystallization orientation.
- the characteristics of the cold-rolled steel sheet for the grain-oriented electrical steel sheet according to this embodiment will be specifically described.
- the cold-rolled steel sheet shown in Figure 2 satisfies the following characteristics.
- the cold-rolled steel sheet for the grain-oriented electrical steel sheet according to this embodiment is The deviation angle from the ideal Goss orientation with the normal direction of the rolling surface as the rotation axis is defined as ⁇ , The deviation angle from the ideal Goss orientation with the direction perpendicular to the rolling as the rotation axis is defined as ⁇ .
- the crystal grains having the angle deviation ⁇ of 10° or less are defined as Goss oriented grains, A 100 mm x 100 mm area on the plate surface is defined as a divided section.
- the area percentage of the divided sections containing at least one Goss oriented grain having a grain size of 5 ⁇ m or more is 30% or more of all the divided sections.
- a cold-rolled steel sheet 1000 mm long can be divided into the above compartments, and the sum of the areas of the compartments containing at least one Goss-oriented grain with a grain size of 5 ⁇ m or more (coarse Goss-oriented grain) can be calculated, and the ratio of this sum to the area of all the compartments can be calculated.
- the above grain size is determined by recognizing a grain boundary as a point where the crystal orientation difference between adjacent measurement points is 1° or more. Also, the above grain size refers to the circle equivalent diameter.
- the angle deviation ⁇ is defined by the deviation angles ⁇ and ⁇ .
- the angle deviation ⁇ is often evaluated by three components, the deviation angles ⁇ , ⁇ , and ⁇ .
- the angle deviation ⁇ is defined by two components, the deviation angles ⁇ and ⁇ , excluding the deviation angle ⁇ , which has a small effect on the magnetic flux density.
- the above-mentioned coarse Goss-oriented grains are defined as Goss-oriented grains having a grain size of 5 ⁇ m or more, but there is no particular upper limit to the grain size.
- the maximum grain size of the coarse Goss-oriented grains may be, for example, 100 ⁇ m.
- At least one coarse Goss-oriented grain (a coarse Goss-oriented grain close to the ideal Goss orientation) is contained within a 100 mm x 100 mm divided section of the cold-rolled steel sheet, and when the total area of the divided sections containing such coarse Goss-oriented grains is 30% or more of the area of all divided sections, the Goss-oriented grains grow in a preferred form during the secondary recrystallization stage, and a grain-oriented electrical steel sheet with good magnetic properties can be obtained.
- the heated spot electrode suppresses heat removal from the steel sheet, promoting the grain growth of the generated Goss orientation grains and promoting the generation of Goss orientation grains that have a size effect suitable for secondary recrystallization and have a crystal orientation close to the ideal Goss orientation.
- the current-carrying electrode has a diameter of 0.5 mm ⁇ to 10 mm ⁇ in equivalent circle diameter, it is easy to ensure a preferable holding time from when the maximum temperature is reached until cooling to 700°C. Under normal laser irradiation or electron beam irradiation conditions, it is difficult to ensure the above-mentioned holding time from when the maximum temperature is reached until cooling to 700°C.
- the divided sections containing at least one coarse Goss-oriented grain are uniformly present throughout the entire cold-rolled steel sheet.
- the above condition does not have to be satisfied over the entire surface of the cold-rolled steel sheet.
- the divided sections containing at least one coarse Goss-oriented grain are unevenly distributed in a part of the cold-rolled steel sheet, as long as they account for 30% or more of the area of all the divided sections, a grain-oriented electrical steel sheet with good magnetic properties can ultimately be obtained.
- the divided sections containing at least one coarse Goss-oriented grain preferably account for 50% or more of the area of all divided sections, more preferably 70% or more of the area, and even more preferably 90% or more of the area.
- the magnetic flux density B8 is improved.
- the fewer the number of locally heated regions in a divided section the larger the grain size after secondary recrystallization.
- magnetic domain control techniques such as laser irradiation or linear groove formation are applied. Therefore, it is preferable to form, for example, an average of three or more locally heated regions, preferably five or more, and more preferably nine or more, in each divided section of 100 mm x 100 mm.
- the cold-rolled steel sheet according to this embodiment When the cold-rolled steel sheet according to this embodiment is used, during secondary recrystallization, among the Goss-oriented grains in the local heating region, the coarse Goss-oriented grains close to the ideal Goss orientation grow preferentially. Therefore, even if the secondary recrystallized grains are not grown large, the steel sheet can be dominated by secondary recrystallized grains close to the ideal Goss orientation.
- the local heating regions are scattered on the steel sheet surface, the size, shape, and arrangement of the crystal grains after secondary annealing can be controlled by appropriately arranging the local heating regions on the steel sheet surface.
- the grain size of the Goss-oriented grains at the end of secondary annealing will be small, and a steel sheet with excellent iron loss can be obtained.
- the crystals close to the ideal Goss orientation grow preferentially, so that good magnetic properties can be obtained despite the small secondary recrystallized grain size.
- the magnetic flux density can be increased while suppressing the coarsening of the secondary recrystallized grain size, so that the magnetic domain width refinement by strain introduction or groove formation can be unnecessary or reduced.
- the magnetic domain refinement effect can be preferably obtained by the grain boundaries that increase with the refinement of the secondary recrystallized grain size, the magnetic domains are refined without applying the conventional magnetic domain control technology. Therefore, since it is not necessary to introduce strain into the steel sheet as in the conventional magnetic domain control technology, it is possible to prevent an increase in magnetostriction ( ⁇ P-P ).
- the grain-oriented electrical steel sheet using the cold-rolled steel sheet according to the present embodiment can be used for applications requiring strain relief annealing at 800 ° C. or more.
- the coarse Goss-oriented grains contained in the divided sections need only be Goss-oriented grains with a grain size of 5 ⁇ m or more.
- the coarse Goss-oriented grains contained in the divided sections are Goss-oriented grains with a grain size of 8 ⁇ m or more.
- the divided sections containing at least one Goss-oriented grain with a grain size of 8 ⁇ m or more account for 30 area% or more of all the divided sections. It is preferable that this divided section account for 50 area% or more of all the divided sections, more preferably 70 area% or more, and even more preferably 90 area% or more.
- the above-mentioned grain size of the Goss orientation can be measured by the EBSD method. If the area to be measured is larger than the area that can be measured by EBSD, the area to be measured can be divided and EBSD measurements can be performed multiple times. For example, the step size for EBSD measurement can be set to 0.5 ⁇ m.
- the grain-oriented electrical steel sheet as a final product may have a chemical composition, in mass fraction, of 2.0% to 7.0% Si, with the remainder being Fe and impurities.
- this grain-oriented electrical steel sheet may contain publicly known optional elements in place of a portion of Fe in order to improve the magnetic properties.
- the lower limit may be 0%.
- the upper limit for the optional elements may be set to a range in which no significant decrease in magnetic flux density or iron loss occurs. The approximate upper limit for each optional element is listed below.
- the chemical composition of the final product, grain-oriented electrical steel sheet (base steel sheet), is, in mass%, as follows: C: 0.005% or less, Si: 2.0 to 7.0%, Mn: 1.00% or less, S and Se: 0.015% or less in total; Al: 0.065% or less, N: 0.005% or less, Nb, V, Mo, Ta, and W: 0.050% or less in total; Cu: 0.40% or less, Bi: 0.010% or less, B: 0.080% or less, P: 0.50% or less, Ti: 0.015% or less, Sn: 0.10% or less, Sb: 0.10% or less, Cr: 0.30% or less, Ni: 1.00% or less.
- the total content of S and Se means that at least one of S and Se is included, and that the total content is the total content of the elements.
- the total content of one or more of Nb, V, Mo, Ta, and W means that at least one of Nb, V, Mo, Ta, and W is included, and that the total content is the total content of the elements.
- the decarburization annealing and purification annealing during secondary recrystallization cause relatively large changes in the chemical composition (reduction in content).
- the content can be reduced to 50 ppm or less, and if purification annealing is carried out sufficiently, it can reach a level that cannot be detected by general analysis (1 ppm or less).
- impurities refer to elements that are inevitably mixed in from raw materials such as ore and scrap, or from the manufacturing environment, when industrially manufacturing steel sheets.
- the upper limit of the total impurity content may be, for example, 5%.
- the above chemical composition may be measured using a general analytical method for steel.
- the chemical composition may be measured using ICP-AES (Inductively Coupled Plasma-Atomic Emission Spectrometry).
- ICP-AES Inductively Coupled Plasma-Atomic Emission Spectrometry
- the chemical composition is determined by measuring a 35 mm square test piece taken from the steel plate using an ICP-AES or similar (measuring device) under conditions based on a previously prepared calibration curve.
- C and S may be measured using the combustion-infrared absorption method
- N may be measured using the inert gas fusion-thermal conductivity method.
- the chemical composition of the cold-rolled steel sheet according to this embodiment contains, for example, the following elements:
- the cold-rolled steel sheet according to this embodiment has a chemical composition, in mass%, C: 0 to 0.0850%, Si: 2.0 to 7.0%, Mn: 0.05-1.0%, S and Se: 0.003 to 0.035% in total, Al: 0.010-0.0650%, N: 0 to 0.012%, Nb, V, Mo, Ta, and W: 0 to 0.050% in total; Cu: 0 to 0.40%, Bi: 0 to 0.010%, B: 0 to 0.080%, P: 0-0.50%, Ti: 0 to 0.0150%, Sn: 0 to 0.10%, Sb: 0 to 0.10%, Cr: 0 to 0.30%, Ni: 0 to 1.0% and the remainder being Fe and impurities.
- C 0-0.0850% Carbon (C) is an effective element for controlling the primary recrystallized structure in the manufacturing process, but if its content in the final product is excessive, it will have a detrimental effect on the magnetic properties.
- the preferred upper limit of the C content is 0.085% or less.
- the preferred upper limit of the C content is 0.075%.
- C is purified in the decarburization annealing process and the final annealing process described below, and is added after the final annealing process to suppress the occurrence of magnetic aging. In order to effectively suppress magnetic aging, the C content is preferably 0.003% or less, and more preferably 0.002% or less. Considering the productivity in production, the lower limit of the C content may be more than 0%.
- the C content depends on the decarburization annealing time, etc., in consideration of the annealing cost, etc., it is practically preferable to set the lower limit at 0%. It may be 0.0001%. Furthermore, if the manufacturing cost is taken into consideration, it may be 0.0005%.
- Si 2.0-7.0%
- Silicon (Si) increases the electrical resistance of grain-oriented electrical steel sheets and reduces iron loss. If the Si content is less than 2.0%, ⁇ transformation occurs during final annealing, and the crystallization of the grain-oriented electrical steel sheets is reduced. On the other hand, if the Si content exceeds 7.0%, the cold workability decreases and cracks tend to occur during cold rolling.
- the upper limit of the Si content is preferably 4.5%, and more preferably 4.0%.
- Mn 0.05-1.0%
- Manganese (Mn) combines with S or Se to produce MnS or MnSe, and functions as an inhibitor.
- Mn is contained, the Mn content is within the range of 0.05 to 1.0%.
- the secondary recrystallization is stabilized.
- part of the inhibitor function is performed by nitrides of Nb group elements (Nb, V, Mo, Ta, and W).
- the strength of MnS or MnSe as a general inhibitor is controlled to be weak, and therefore the upper limit of the Mn content is preferably 0.50%, and more preferably 0.20%.
- S and Se 0.003 to 0.035% in total Sulfur (S) and selenium (Se) combine with Mn to produce MnS or MnSe, which functions as an inhibitor.
- S and Se When at least one of S and Se is contained, if the total content of S and Se is 0.003 to 0.035%, secondary recrystallization is stable. It is possible to use nitrides of Nb group elements to play a part of the inhibitor function. In this case, the strength of MnS or MnSe as a general inhibitor is controlled to be weak. For this reason, in the case of a manufacturing method using low-temperature slab heating, the preferred upper limit of the total content of S and Se is 0.025%, and more preferably 0.010%. If S and Se remain after final annealing, they form compounds and deteriorate iron loss. Therefore, it is preferable to reduce S and Se as much as possible by purification during final annealing.
- the total content of S and Se means that at least one of S and Se is included, and is the total content.
- Al 0.010-0.0650%
- Aluminum (Al) combines with N to precipitate as (Al,Si)N, and functions as an inhibitor.
- the Al content is within the range of 0.010 to 0.0650%.
- AlN formed as an inhibitor by nitriding, which will be described later expands the secondary recrystallization temperature range, and secondary recrystallization is particularly stable in the high temperature range. Therefore, the Al content is 0.010 to 0.0650
- the lower limit of the Al content is preferably 0.020%, and more preferably 0.025%.
- the upper limit of the Al content is preferably 0.040%. and more preferably 0.035%.
- N 0-0.012% Nitrogen (N) combines with Al to function as an inhibitor. Since N can be incorporated by nitriding during the manufacturing process, no lower limit is specified. For example, the lower limit of the N content is set to more than 0%. On the other hand, when N is contained, if the N content exceeds 0.012%, blisters, which are a type of defect, are likely to occur in the steel sheet.
- the upper limit of the N content is preferably 0.010%, and more preferably 0.009%. N is purified in the final annealing process, and the N content becomes 0.005% or less after the final annealing process.
- the balance of the above chemical composition consists of Fe and impurities.
- impurities refers to elements that are mixed in from raw materials such as ore and scrap during industrial production of steel, or from the production environment, etc.
- the upper limit of the total impurity content may be, for example, 5%.
- Nb, V, Mo, Ta, and W 0 to 0.050%
- the total content of Nb (niobium), V (vanadium), Mo (molybdenum), Ta (tantalum), and W (tungsten) may be 0.050% or less.
- Nb group elements one or more of Nb, V, Mo, Ta, and W
- the effect of improving B8 is exhibited.
- the Nb group elements remain excessively in the base steel sheet, it may have a negative effect on the magnetic properties. Therefore, the total content of Nb, V, Mo, Ta, and W may be 0.050% or less.
- the total content of Nb group elements is 0.030% or less (preferably 0.003% or more and 0.030% or less), it is preferable because secondary recrystallization is started at an appropriate timing.
- the orientation of the secondary recrystallized grains that occur becomes very favorable, and it can be finally controlled to a structure favorable for the magnetic properties.
- Nb and Ta are preferable because their effects are strong.
- the lower limit is preferably 0.003%.
- the total content of Nb group elements is more preferably 0.004 to 0.020%. Even more preferably, it is 0.005 to 0.010%.
- the total content of Nb group elements means the total content including at least one of Nb, V, Mo, Ta, and W.
- the cold-rolled steel sheet according to this embodiment contains, as optional elements, in mass%: Cu: 0 to 0.40%, Bi: 0 to 0.010%, B: 0 to 0.080%, P: 0-0.50%, Ti: 0 to 0.0150%, Sn: 0 to 0.10%, Sb: 0 to 0.10%, Cr: 0 to 0.30%, Ni: 0 to 1.0% may contain at least one of the following. Since these optional elements may be contained according to known purposes, there is no need to set a lower limit for the content of the optional elements, and the lower limit may be 0%.
- the chemical composition of the cold-rolled steel sheet according to this embodiment can be measured by the above-mentioned analytical method, in the same way as the chemical composition of the grain-oriented electrical steel sheet as the final product.
- the method for manufacturing the cold-rolled steel sheet according to this embodiment is not limited to the method described below.
- the manufacturing method described below is one example for manufacturing the cold-rolled steel sheet according to this embodiment.
- the steps and quantitative conditions for each step shown below are examples adopted to demonstrate the feasibility of this embodiment, and this embodiment is not limited to these steps and quantitative values.
- the manufacturing method for cold-rolled steel sheet according to this embodiment may adopt various conditions as long as they do not deviate from the gist of this embodiment and achieve the purpose of this embodiment.
- the manufacturing method of the cold-rolled steel sheet according to this embodiment can apply the conventional known manufacturing method of grain-oriented electrical steel sheet as a basic process.
- examples of conventional manufacturing methods of grain-oriented electrical steel sheet include a manufacturing method in which inhibitors such as MnS and AlN are formed by high-temperature slab heating, and a manufacturing method in which AlN inhibitors are formed by low-temperature slab heating and nitriding treatment.
- the manufacturing method of the cold-rolled steel sheet according to this embodiment is not limited to a specific manufacturing method. Below, a method of applying nitriding treatment as a low-temperature slab heating process will be described.
- a slab is prepared.
- An example of a method for producing a slab is as follows. Molten steel is produced (smelted). A slab is produced using the molten steel. The slab may be produced by a continuous casting method. An ingot may be produced using the molten steel, and the ingot may be bloomed to produce a slab.
- the thickness of the slab is not particularly limited. The thickness of the slab is, for example, 150 to 350 mm. The thickness of the slab is preferably 220 to 280 mm. As the slab, a so-called thin slab having a thickness of 10 to 70 mm may be used. When a thin slab is used, rough rolling before finish rolling can be omitted in the hot rolling process.
- the above slab may contain the following elements in its chemical composition:
- Carbon (C) is an effective element for controlling the primary recrystallized structure in the manufacturing process, but if its content in the final product is excessive, it will have a detrimental effect on the magnetic properties.
- the preferred upper limit of the C content is 0.075%.
- C is purified in the decarburization annealing process and the finish annealing process to be 0.005% or less.
- the lower limit of the C content may be more than 0%, or may be 0.001%.
- Si 2.0-7.0%
- Silicon (Si) increases the electrical resistance of grain-oriented electrical steel sheets and reduces iron loss. If the Si content is less than 2.0%, ⁇ transformation occurs during final annealing, and the crystallization of the grain-oriented electrical steel sheets is reduced. On the other hand, if the Si content exceeds 7.0%, the cold workability decreases and cracks tend to occur during cold rolling.
- the upper limit of the Si content is preferably 4.5%, and more preferably 4.0%.
- Mn 0.05-1.00%
- Manganese (Mn) combines with S or Se to produce MnS or MnSe, and functions as an inhibitor.
- Mn is contained, the Mn content is within the range of 0.05 to 1.00%.
- the secondary recrystallization is stable. It is possible for part of the inhibitor function to be performed by a nitride of an Nb group element. In this case, the strength of MnS or MnSe as a general inhibitor is Therefore, the upper limit of the Mn content is preferably 0.50%, and more preferably 0.20%.
- At least one of S and Se 0.003 to 0.035% in total Sulfur (S) and selenium (Se) combine with Mn to produce MnS or MnSe, which functions as an inhibitor.
- S and Se When at least one of S and Se is contained, if the total content of S and Se is 0.003 to 0.035%, secondary recrystallization is stable. It is possible for a part of the inhibitor function to be borne by a nitride of an Nb group element. In this case, the strength of MnS or MnSe as a general inhibitor is controlled to be weak. For this reason, the preferred upper limit of the total content of S and Se is 0.025%, and more preferably 0.010%. If S and Se remain after the final annealing, they form compounds and deteriorate the iron loss. Therefore, it is preferable to reduce S and Se as much as possible by purification during the final annealing.
- the total content of S and Se means that at least one of S and Se is included, and is the total content.
- Al 0.010-0.065%
- Aluminum (Al) combines with N to precipitate as (Al,Si)N, and functions as an inhibitor.
- the Al content is within the range of 0.010 to 0.065%.
- AlN formed as an inhibitor by nitriding, which will be described later expands the secondary recrystallization temperature range, and secondary recrystallization is particularly stable in the high temperature range. Therefore, the Al content is 0.010 to 0.065
- the lower limit of the Al content is preferably 0.020%, and more preferably 0.025%.
- the upper limit of the Al content is preferably 0.040%. and more preferably 0.035%.
- N 0.012% or less Nitrogen (N) combines with Al to function as an inhibitor. Since N can be contained by nitriding during the manufacturing process, no lower limit is specified. For example, the lower limit of the N content may be more than 0%, or may be 0.001%. On the other hand, when N is contained, if the N content exceeds 0.012%, blisters, which are a type of defect, tend to occur in the steel sheet. The preferred upper limit of the N content is 0.010%, and more preferably 0.009%. N is purified in the final annealing process, and becomes 0.005% or less after the final annealing process.
- the balance of the above chemical composition consists of Fe and impurities.
- impurities refers to elements that are mixed in from raw materials such as ore and scrap during industrial production of steel, or from the production environment, etc.
- the upper limit of the total impurity content may be, for example, 5%.
- the above-mentioned chemical composition may contain known optional elements in place of part of Fe, taking into consideration not only solving manufacturing problems, but also strengthening the inhibitor function through compound formation and the effect on magnetic properties.
- optional elements that may be contained in place of part of Fe include the following elements:
- Nb group elements 0.050% or less
- the total content of Nb group elements (one or more of Nb, V, Mo, Ta, and W) may be 0.050% or less.
- the total content of Nb group elements is 0.030% or less, since secondary recrystallization is started at an appropriate timing.
- the orientation of the secondary recrystallized grains generated becomes very favorable, and the structure can be finally controlled to be favorable for magnetic properties.
- Nb and Ta have a strong effect and are preferable.
- the total content of Nb group elements is more preferably 0.004 to 0.020%. Even more preferably, it is 0.005 to 0.010%.
- the total content of Nb group elements means the total content including at least one of Nb, V, Mo, Ta, and W.
- the slab also contains, as optional elements, in mass %: Cu: 0.40% or less, Bi: 0.010% or less, B: 0.080% or less, P: 0.50% or less, Ti: 0.015% or less, Sn: 0.10% or less, Sb: 0.10% or less, Cr: 0.30% or less, Ni: 1.00% or less. Since these optional elements may be contained according to known purposes, there is no need to set a lower limit for the content of the optional elements, and the lower limit may be 0%.
- the chemical composition of the above slabs can be measured by the above analytical method, just like the chemical composition of the final product, grain-oriented electrical steel sheet.
- the hot rolling process is a process in which a slab heated to a predetermined temperature (e.g., 1100 to 1400°C) is hot-rolled to obtain a hot-rolled steel sheet.
- a predetermined temperature e.g. 1100 to 1400°C
- the silicon steel material (slab) heated in the heating process is roughly rolled, and then finish-rolled to obtain a hot-rolled steel sheet with a predetermined thickness, for example, 1.8 to 3.5 mm. After the finish rolling is completed, the hot-rolled steel sheet is coiled at a predetermined temperature.
- the slab heating temperature should be 1100°C to 1280°C.
- the hot-rolled sheet annealing process is a process in which the hot-rolled steel sheet obtained in the hot rolling process is annealed under a predetermined temperature condition (for example, at 750 to 1200 ° C for 30 seconds to 10 minutes) to obtain an annealed steel sheet.
- Hot-rolled sheet annealing is generally performed to control the steel sheet structure such as the recrystallization rate, residual strain, and crystal grain size by annealing the hot-rolled steel sheet after the hot rolling process, and to preferably adjust the precipitate form in the steel.
- a high-temperature slab heating process it is a process for finally controlling the form of precipitates such as AlN, and conditions are adjusted so that they precipitate uniformly and finely.
- the hot-rolled sheet annealing for example, after heating the steel sheet to 1050 ° C to 1150 ° C, in order to properly precipitate AlN, etc., it may be cooled slowly to an intermediate temperature (850 ° C to 950 ° C) for 50 to 150 seconds, and then cooled with water.
- an intermediate temperature 850 ° C to 950 ° C
- the cold rolling process is a process in which the annealed steel sheet obtained in the hot-rolled sheet annealing process is subjected to one cold rolling or multiple cold rolling (two or more times) via annealing (intermediate annealing) to obtain a cold-rolled steel sheet having a thickness of, for example, 0.10 to 0.50 mm.
- the interpass temperature of the cold rolling may be set to about 100° C. to 300° C.
- Total cold rolling rate (%) (1 - thickness of steel plate after cold rolling / thickness of steel plate before cold rolling) x 100
- local rapid heating is performed on the cold-rolled steel sheet after the cold rolling process to form a local heating region.
- the rapid heating method is not particularly limited as long as it can locally heat the steel sheet.
- a method of heating by contacting a spot electrode with the front and back surfaces of the steel sheet and passing an electric current through the steel sheet a method of heating by irradiating the surface of the steel sheet with laser light or an electron beam, a method of locally heating by induction heating, a method of heating by contacting a hot piece, etc. can be adopted.
- each local heating region can be a dot-like region with a diameter of about 10 ⁇ m to 10 mm, or a linear region with a width of about 10 ⁇ m to 10 mm.
- the electrode used for electric heating may be a circular electrode as described above, or a linear electrode.
- the minimum diameter and minimum width depend on the shape of the spot electrode and the technology for reducing the focused diameter of the laser light or electron beam. In principle, it is possible to further reduce the size of the locally heated region, but considering that the current size of the nuclei of recrystallized grains is about 1 ⁇ m, it is believed that an effect can be obtained if the size of the locally heated region is 1 ⁇ m or more. However, since the objective of this embodiment is to form Goss-oriented grains with a grain size of 5 ⁇ m or more, the above minimum diameter and minimum width should be 10 ⁇ m or more.
- the size of the locally heated region if the maximum diameter or maximum width exceeds 10 mm, the area ratio of Goss-oriented grains with relatively large angle deviations ⁇ and ⁇ that cannot grow outside the locally heated region increases. In this case, it becomes difficult to obtain the effect of local rapid heating.
- the heating rate should be 500°C/sec or more in the center of the locally heated region as viewed in the thickness direction and at 1/5 of the thickness of the steel plate. If the heating rate in the above region is 500°C/sec or more, the structure of the locally heated region can be preferably controlled to a recovered structure or a recrystallized structure.
- the above heating rate is preferably 2000°C/sec or more, and more preferably 10000°C/sec or more.
- the upper limit of the above heating rate is not particularly limited, and may be, for example, 1,000,000°C/sec.
- the above heating rate in conjunction with the heating rate during decarburization annealing, which will be described later.
- the heating rate during decarburization annealing is faster than the heating rate during localized rapid heating, it is difficult to obtain the desired effect. Therefore, although it depends on the magnitude of the heating rate, it is preferable to set the heating rate during localized rapid heating to be equal to or greater than the heating rate during decarburization annealing.
- the 1/5 part of the thickness of the steel plate mentioned above refers to a depth equivalent to 1/5 of the thickness of the steel plate from the surface of the steel plate in the thickness direction.
- the maximum temperature reached should be 700°C or higher in the center of the locally heated region when viewed from the plate thickness direction and at 1/5 of the plate thickness of the steel plate. If the maximum temperature reached in the above region is 700°C or higher, the structure of the locally heated region can be preferably controlled to a recovered structure or a recrystallized structure.
- the above maximum temperature reached is preferably 800°C or higher, and more preferably 900°C or higher.
- the above maximum temperature reached should be below the melting point of the steel plate, for example, 1400°C or lower.
- the holding time from reaching the maximum temperature to cooling to 700°C at the center of the locally heated region as viewed from the thickness direction and at 1/5 of the thickness of the steel plate should be 0.1 seconds or more. If the holding time in the above region is 0.1 seconds or more, the structure of the locally heated region can be preferably controlled to a recovered structure or a recrystallized structure.
- the holding time is preferably 0.2 seconds or more, more preferably 0.3 seconds or more, and even more preferably 0.4 seconds or more.
- there is no particular limit to the upper limit of the holding time and it may be, for example, 10 seconds or less.
- the holding time from reaching the maximum temperature to cooling to 700°C has a fundamental effect on the formation of coarse Goss orientation grains close to the ideal Goss orientation.
- the method of local rapid heating is not particularly limited.
- local rapid heating may be performed by spot electrical current heating, laser irradiation, or electron beam irradiation.
- it is sufficient to control the heating rate, maximum temperature, and holding time described above so as to satisfy the above.
- a person skilled in the art can combine the various conditions of the local rapid heating method to control the desired heating rate, maximum temperature, and holding time.
- a person skilled in the art can perform a heat conduction analysis using the finite element method to control the heating rate and maximum temperature reached in the center of the localized heating area when viewed from the plate thickness direction and at 1/5 of the plate thickness of the steel plate.
- a person skilled in the art can control the above-mentioned holding time by adjusting the heat removal conditions after the maximum temperature is reached. For example, in the case of spot current heating, the electrode holding time after current is controlled, or the shape of the spot electrode can be changed to a shape suitable for heat removal.
- the irradiation speed can be adjusted, or the shape of the irradiation area can be changed to an ellipse or the like to gradient the irradiation energy from the center to the outer edge of the irradiation area.
- the heating by laser irradiation preferentially heats only the vicinity of the irradiated steel sheet surface, and the inside of the steel sheet is not easily heated.
- the heating by laser irradiation is non-contact heating, the heat is removed quickly after heating, and the temperature is not easily maintained. Therefore, when performing laser irradiation heating as local rapid heating, in order to recover or recrystallize the cold-worked structure in the laser irradiated region, it is necessary to control the conditions so that not only the surface of the steel sheet but also the inside of the steel sheet is heated, and the cooling rate is slowed down to relatively coarsen the subgrain structure in the laser irradiated region.
- the laser irradiation conditions for performing local rapid heating are completely different from the laser irradiation conditions for performing magnetic domain refinement. For example, even if the laser irradiation conditions for performing magnetic domain refinement (usually 0.5 to 50 mJ/mm 2 ) are applied to this embodiment, the structure of the locally heated region is not favorably controlled, and coarse Goss orientation grains close to the ideal Goss orientation are not formed in the cold-rolled steel sheet. The same applies to electron beam irradiation. Even if the electron beam irradiation conditions for magnetic domain refinement are applied to this embodiment, the structure of the locally heated region is not favorably controlled, and coarse Goss-oriented grains close to the ideal Goss orientation are not formed in the cold-rolled steel sheet.
- the above steps allow the manufacture of the cold-rolled steel sheet for grain-oriented electrical steel sheet according to this embodiment.
- the cold-rolled steel sheet according to this embodiment which is manufactured by controlling the conditions of each step in a complex and inseparable manner, has coarse Goss-oriented grains formed in a preferred form within the steel sheet.
- Decarburization annealing process In the decarburization annealing process, the cold-rolled steel sheet after the local rapid heating process is subjected to decarburization annealing (primary annealing). This decarburization annealing increases the frequency of Goss-oriented grains formed in the local heating region, increases the grain size of the Goss-oriented grains, and favorably grows coarse Goss-oriented grains having an orientation close to the ideal Goss orientation.
- the decarburization annealing conditions may be, for example, an annealing temperature of 700 to 900°C and an annealing time of 1 to 3 minutes.
- C contained in the cold-rolled steel sheet is removed.
- Decarburization annealing is preferably performed in a moist atmosphere in order to remove "C" contained in the cold-rolled steel sheet.
- the primary recrystallized grain size is not particularly limited, but is preferably 8 to 30 ⁇ m.
- the amount of decarbonation and the state of the surface oxide layer affect the formation of the glass film, so in decarburization annealing, the degree of oxidation (PH 2 O/PH 2 ) in the annealing atmosphere (furnace atmosphere) may be appropriately adjusted.
- Nitriding is an effective treatment in a low-temperature slab heating process in which the slab heating temperature is 1280°C or less, and is an important step for adjusting the strength of the inhibitor in secondary recrystallization. Nitriding increases the nitrogen content of the steel sheet by about 40 to 200 ppm between the start of the decarburization treatment and the start of secondary recrystallization in the finish annealing.
- Examples of nitriding include a treatment of annealing in an atmosphere containing a gas with nitriding ability such as ammonia, and a treatment of finish annealing a decarburized annealed steel sheet coated with an annealing separator containing a powder with nitriding ability such as MnN.
- the amount of nitriding after the nitriding treatment is preferably 130 to 350 ppm, and more preferably 150 to 250 ppm.
- the annealing separator application process is a process of applying an annealing separator to the decarburized annealed steel sheet.
- an annealing separator mainly composed of MgO can be used as the annealing separator.
- the decarburized annealed steel sheet after application of the annealing separator is wound into a coil and finish-annealed in the next finish-annealing process.
- the final annealing process is a process in which the decarburized annealed steel sheet coated with the annealing separator is subjected to final annealing (secondary annealing) to cause secondary recrystallization.
- second annealing final annealing
- the growth of the primary recrystallized grains is suppressed by an inhibitor, and the secondary recrystallization is allowed to proceed, thereby preferentially growing ⁇ 100 ⁇ 001> oriented grains and dramatically improving the magnetic flux density.
- the heating rate during the heating process of the final annealing step is not particularly limited.
- the temperature may be increased at a heating rate of 3 to 20°C/hour.
- slow heating may be performed in the temperature range of 1000°C to 1200°C during the temperature increase.
- the heating rate in the temperature range of 1000°C to 1200°C during the temperature increase is preferably 3 to 12°C/hour, more preferably 3 to 9°C/hour, and even more preferably 3 to 7°C/hour.
- the temperature increase may be stopped once during the heating process of the final annealing step and the temperature may be held.
- the temperature increase may be stopped once in the temperature range of 1050°C to 1100°C during the temperature increase, and the temperature may be held for 5 hours to 15 hours.
- adjusting the heating rate in the secondary recrystallization temperature range affects the decomposition rate of the inhibitor and can improve the magnetic flux density.
- the holding process may involve holding the material in a temperature range of 1000°C to 1300°C for 10 hours to 60 hours.
- the atmosphere during the final annealing may be, for example, a nitrogen atmosphere or a mixed atmosphere of nitrogen and hydrogen.
- a coating solution containing phosphoric acid or a phosphate, chromic anhydride or a chromate, and colloidal silica is applied to the steel sheet and baked (for example, at 350°C to 1150°C for 5 to 300 seconds) to form an insulating coating. do.
- the grain-oriented electrical steel sheet may be subjected to a magnetic domain refinement treatment for forming localized micro-distorted regions or grooves by a known method such as laser, plasma, mechanical method, etching, etc.
- a magnetic domain refinement treatment for forming localized micro-distorted regions or grooves by a known method such as laser, plasma, mechanical method, etching, etc.
- the grain-oriented electrical steel sheet manufactured using the cold-rolled steel sheet according to the present embodiment has excellent magnetic flux density, but the coarsening of secondary recrystallized grains is suppressed, so that the magnetic domains are refined even without the magnetic domain refinement treatment.
- the conditions in the examples are one example of conditions adopted to confirm the feasibility and effects of the present invention, and the present invention is not limited to this one example of conditions.
- Various conditions can be adopted in the present invention as long as they do not deviate from the gist of the present invention and the object of the present invention is achieved.
- the slabs were heated to 1150°C and subjected to hot rolling to obtain hot-rolled steel sheets with a thickness of 2.6 mm.
- the hot-rolled steel sheets were then heated to 1100°C and subsequently annealed at 900°C for hot-rolled sheet annealing, after which pickling was performed to remove the scale formed on the surface.
- These steel sheets were subjected to one cold rolling or multiple cold rolling with intermediate annealing in between to obtain cold-rolled steel sheets with a final thickness of 0.22 mm.
- the above cold-rolled steel sheets were subjected to localized rapid heating under the conditions shown in Tables 3 to 7.
- spot current heating a copper electrode with a diameter of 3 mm was used in the contact area with the steel sheet, and the electrode shape, electrode pressure, current, current duration, and electrode holding time after current were varied in a composite manner to control the heating rate, maximum temperature, and holding time from reaching the maximum temperature until cooling to 700°C (holding time above 700°C).
- the laser heating a fiber laser was used, and the diameter of the focused spot of the laser light in the rolling direction (i.e., the diameter including 86% of the laser output) was set to 30 ⁇ m (except for Tests No. 85 and No. 86).
- the heating rate, maximum temperature, and holding time above 700°C were controlled by varying the laser irradiation energy density, laser scanning speed, and shape of the laser irradiation area in a composite manner.
- Those skilled in the art can combine the conditions of the localized rapid heating method to control the desired heating rate, maximum temperature, and holding time above 700°C.
- test No. 83 the laser beam was elongated in the scanning direction, and the holding time from reaching the maximum temperature to cooling to 700 ° C. during local rapid heating was controlled to 0.2 seconds, so that coarse Goss orientation grains having an orientation close to the ideal Goss orientation were formed in the locally heated area.
- test No. 84 general laser irradiation conditions for magnetic domain refinement were applied.
- the focusing spot diameter was set to 0.5 mm
- the laser irradiation energy density was set to 2.0 J/mm 2
- the laser beam irradiation portion was controlled so that it would eventually become the grain boundary of the secondary recrystallized grain.
- the focusing spot diameter was set to 0.5 mm
- the laser irradiation energy density was set to 30.0 J/mm 2
- the laser beam irradiation portion was controlled so that it would finally become the grain boundary of the secondary recrystallized grain.
- the divided sections containing at least one Goss-oriented grain with a grain size of 5 ⁇ m or more were measured based on the above-mentioned method.
- the results are shown in Tables 8 to 12.
- EBSD measurements were performed on a surface parallel to the steel sheet surface and 20 ⁇ m in the sheet thickness direction. From the EBSD IQ value, it was confirmed that the crystal structure of the locally heated region was a recrystallized structure and a recovered structure, and that the crystal structure of the non-locally heated region other than the locally heated region was a processed structure.
- the localized heating conditions “Linear or dotted” indicate the shape of the localized heated area on the surface of the cold-rolled steel sheet
- the localized heating conditions “Rolling direction spacing” and “Width direction spacing” indicate the spacing in the rolling direction and the direction perpendicular to the rolling direction at which the localized heated areas are arranged on the surface of the cold-rolled steel sheet.
- the localized heated areas are arranged at equal intervals in the rolling direction and the direction perpendicular to the rolling direction. For example, if both the "Rolling direction spacing" and the "Width direction spacing" are 100 mm or less, localized heated areas are arranged in all divided sections.
- the "locally heated section ratio" of the local heating conditions represents the area ratio of the divided sections in which the locally heated areas are located on the plate surface of the cold-rolled steel plate.
- a 100 mm x 100 mm area on the plate surface is defined as a divided section, and when it is confirmed in at least 100 divided sections whether a locally heated area is located within this divided section, the sum of the areas of the divided sections in which the locally heated areas are located divided by the area of all divided sections corresponds to the "locally heated section ratio," and the value is shown as a percentage in the table.
- the "area ratio of the divided sections containing Goss oriented grains of 5 ⁇ m or more" of the manufacturing results represents the area ratio of the divided sections containing coarse Goss oriented grains on the sheet surface of the cold-rolled steel sheet.
- the sum of the areas of the divided sections containing coarse Goss oriented grains divided by the area of all the divided sections corresponds to the "area ratio of the divided sections containing Goss oriented grains of 5 ⁇ m or more," and the value is shown as a percentage in the table.
- almost no Goss oriented grains of 5 ⁇ m or more were observed in the matrix portion other than the locally heated region (non-locally heated region).
- the produced cold-rolled steel sheets were subjected to decarburization annealing under the conditions shown in Tables 8 to 12.
- the degree of oxidation (PH 2 O/PH 2 ) in the annealing atmosphere (furnace atmosphere) was set to 0.13.
- the decarburized annealed steel sheet produced was subjected to nitriding treatment at 750°C in a nitrogen-hydrogen-ammonia atmosphere to set the steel sheet nitrogen content to 220 ppm. Furthermore, an annealing separator mainly composed of MgO was applied, and finish annealing was performed. In the finish annealing, the steel sheet was heated to 1000°C (the “Step" below is 1070°C) at a heating rate of 15°C/hour in a mixed atmosphere of hydrogen and nitrogen, and then heated to 1200°C under any of the following conditions, and held at 1200°C for 20 hours in a hydrogen atmosphere.
- the steel sheet After final annealing, the steel sheet is coated with an insulating coating solution made mainly of colloidal silica and phosphate, with chromic anhydride added as needed, and baked to form an insulating coating.
- an insulating coating solution made mainly of colloidal silica and phosphate, with chromic anhydride added as needed, and baked to form an insulating coating.
- the magnetic properties of the grain-oriented electrical steel sheets were measured based on the single sheet magnetic properties test method (SST: Single Sheet Tester) specified in JIS C 2556:2015.
- the magnetic flux density B 8 (T) in the rolling direction of the steel sheet when excited at 800 A/m was measured.
- the magnetic flux density B 8 was judged to pass or fail based on the Si content of the steel sheet and the finish annealing conditions.
- the steel sheets were divided into Steels A to Z, each having a Si content of 3.3 to 3.5%, Steel AA, each having a Si content of 2.5%, and Steel AB, each having a Si content of 4.1%, and compared under the same finish annealing conditions.
- iron loss W 17/50 (W/kg), defined as the power loss per unit weight (1 kg) of the steel sheet, was measured under conditions of an AC frequency of 50 Hz and an excitation magnetic flux density of 1.7 T.
- the cold-rolled steel sheets according to the present invention had the "area ratio of divided sections containing Goss-oriented grains of 5 ⁇ m or more" preferably controlled. All of these examples according to the present invention, as grain-oriented electrical steel sheets, showed excellent magnetic flux density despite the suppression of coarsening of the secondary recrystallized grain size. Furthermore, because the grain-oriented electrical steel sheets had suppressed coarsening of the secondary recrystallized grain size, they also had excellent iron loss.
- the area ratio of the divided sections that contained at least one Goss-oriented grain with a grain size of 8 ⁇ m or more was the same as the area ratio of the divided sections that contained at least one Goss-oriented grain with a grain size of 5 ⁇ m or more.
- the comparative cold-rolled steel sheets did not have the "area ratio of divided sections containing Goss-oriented grains of 5 ⁇ m or more" controlled appropriately. These comparative examples did not provide a desirable magnetic flux density as grain-oriented electrical steel sheets.
- a cold-rolled steel sheet for grain-oriented electrical steel sheet that can increase the magnetic flux density.
- a cold-rolled steel sheet for grain-oriented electrical steel sheet that can increase the magnetic flux density while suppressing the coarsening of secondary recrystallized grains. Therefore, it has a high industrial applicability.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Physics & Mathematics (AREA)
- Electromagnetism (AREA)
- Thermal Sciences (AREA)
- Crystallography & Structural Chemistry (AREA)
- Manufacturing & Machinery (AREA)
- Dispersion Chemistry (AREA)
- Power Engineering (AREA)
- Manufacturing Of Steel Electrode Plates (AREA)
- Soft Magnetic Materials (AREA)
Abstract
Description
本願は、2023年6月29日に、日本に出願された特願2023-106555号に基づき優先権を主張し、その内容をここに援用する。
即ち、従来の工程制御条件では、ゴス方位粒の存在頻度とゴス方位粒に蚕食されやすい対応方位粒の存在頻度とを独立に制御することができていなかった。
θ=(α2+β2+γ2)1/2 (式1)
圧延面法線方向を回転軸とする理想ゴス方位からのずれ角をαと定義し、
圧延直角方向を回転軸とする理想ゴス方位からのずれ角をβと定義し、
板面上の測定点で測定する結晶方位のずれ角を(α β)と表し、
前記測定点での角度偏差をφ=(α2+β2)1/2と定義し、
前記角度偏差φが10°以下である結晶粒をゴス方位粒と定義し、
板面上の100mm×100mmの領域を分割区画と定義し、
前記分割区画内に前記ゴス方位粒が含まれるかを、少なくとも100区画の分割区画で確認したとき、
5μm以上の粒径をもつゴス方位粒が少なくとも1つ含まれる分割区画が、すべての分割区画に対して、30面積%以上である。
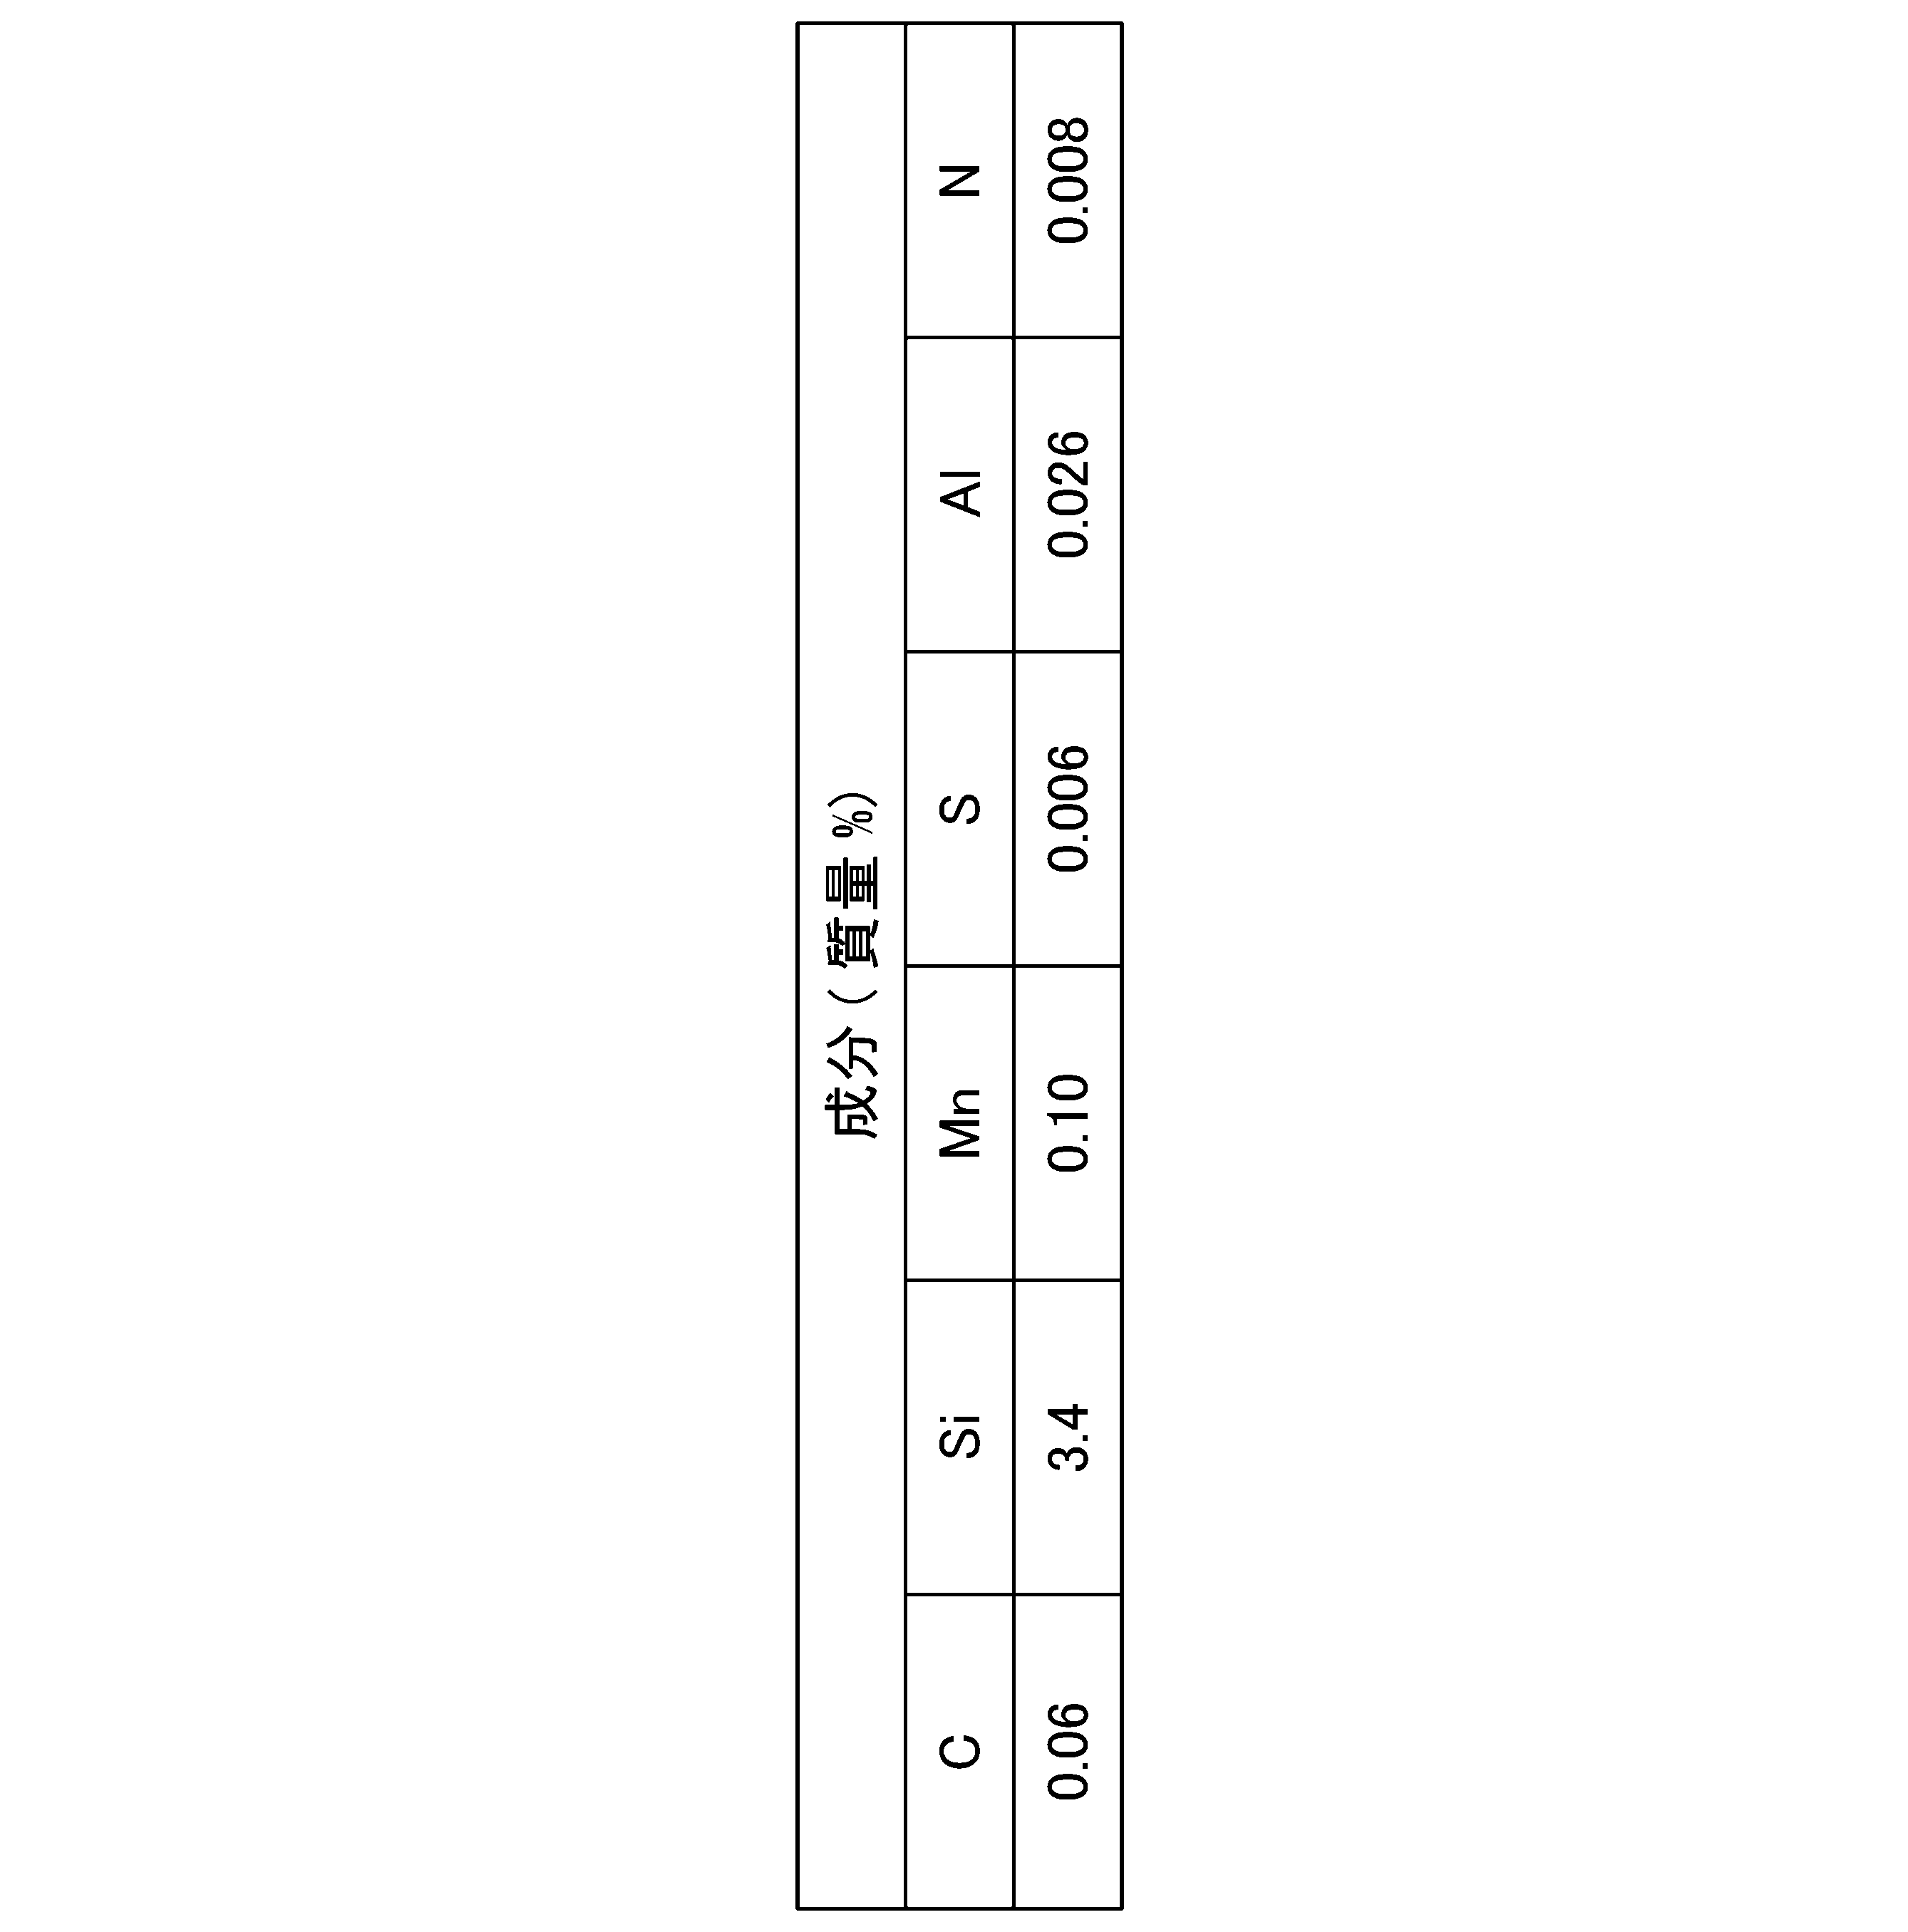
圧延面法線方向を回転軸とする理想ゴス方位からのずれ角をαと定義し、
圧延直角方向を回転軸とする理想ゴス方位からのずれ角をβと定義し、
板面上の測定点で測定する結晶方位のずれ角を(α β)と表し、
上記測定点での角度偏差をφ=(α2+β2)1/2と定義し、
上記角度偏差φが10°以下である結晶粒をゴス方位粒と定義し、
板面上の100mm×100mmの領域を分割区画と定義し、
上記分割区画内に上記ゴス方位粒が含まれるかを、少なくとも100区画の分割区画で確認したとき、
5μm以上の粒径をもつゴス方位粒が少なくとも1つ含まれる分割区画が、すべての分割区画に対して、30面積%以上となる。
最終製品としての方向性電磁鋼板は、化学組成として、質量分率で、Si:2.0%~7.0%を含有し、残部がFeおよび不純物からなればよい。
C:0.005%以下、
Si:2.0~7.0%、
Mn:1.00%以下、
S及びSe:合計で0.015%以下、
Al:0.065%以下、
N:0.005%以下、
Nb、V、Mo、Ta、及びW:合計で、0.050%以下、
Cu:0.40%以下、
Bi:0.010%以下、
B:0.080%以下、
P:0.50%以下、
Ti:0.015%以下、
Sn:0.10%以下、
Sb:0.10%以下、
Cr:0.30%以下、
Ni:1.00%以下
の少なくとも1種を含有してもよい。
C:0~0.0850%、
Si:2.0~7.0%、
Mn:0.05~1.0%、
S及びSe:合計で0.003~0.035%、
Al:0.010~0.0650%、
N:0~0.012%、
Nb、V、Mo、Ta、及びW:合計で、0~0.050%、
Cu:0~0.40%、
Bi:0~0.010%、
B:0~0.080%、
P:0~0.50%、
Ti:0~0.0150%、
Sn:0~0.10%、
Sb:0~0.10%、
Cr:0~0.30%、
Ni:0~1.0%
を含有し、残部がFeおよび不純物からなればよい。
炭素(C)は、製造工程においては一次再結晶組織の制御に有効な元素であるものの、最終製品への含有量が過剰であると磁気特性に悪影響を及ぼす。したがって、C含有量は0.085%以下である。C含有量の好ましい上限は0.075%である。Cは、後述の脱炭焼鈍工程及び仕上げ焼鈍工程で純化され、仕上げ焼鈍工程後には磁気時効の発生を抑制するため、0.0050%以下にされることもある。磁気時効を好ましく抑制するために、C含有量は、0.003%以下が好ましく、0.002%以下がさらに好ましい。Cを含む場合、工業生産における生産性を考慮すると、C含有量の下限は0%超であってもよい。ただ、C含有量は脱炭焼鈍時間などに依存するため、焼鈍コスト等を鑑みれば、実際には0.0001%であってもよい。さらに、製造コストを勘案すれば0.0005%でもよい。
シリコン(Si)は、方向性電磁鋼板の電気抵抗を高めて鉄損を低下させる。Si含有量が2.0%未満であれば、仕上げ焼鈍時にγ変態が生じて、方向性電磁鋼板の結晶方位が損なわれてしまう。一方、Si含有量が7.0%を超えれば、冷間加工性が低下して、冷間圧延時に割れが発生しやすくなる。Si含有量の好ましい下限は2.5%であり、さらに好ましくは3.0%である。Si含有量の好ましい上限は4.5%であり、さらに好ましくは4.0%である。
マンガン(Mn)はS又はSeと結合して、MnS、又は、MnSeを生成し、インヒビターとして機能する。Mnを含有させる場合、Mn含有量が0.05~1.0%の範囲内にある場合に、二次再結晶が安定する。なお、インヒビターの機能の一部をNb群元素(Nb、V、Mo、Ta、及びW)の窒化物によって担うことが可能である。この場合は、一般的なインヒビターとしてのMnS、又は、MnSe強度は弱めに制御する。このため、Mn含有量の好ましい上限は0.50%であり、さらに好ましくは0.20%である。
硫黄(S)及びセレン(Se)は、Mnと結合して、MnS又はMnSeを生成し、インヒビターとして機能する。S及びSeの少なくとも一方を含有させる場合、S及びSeの含有量が合計で0.003~0.035%であれば、二次再結晶が安定する。なお、インヒビターの機能の一部をNb群元素の窒化物によって担うことが可能である。この場合は、一般的なインヒビターとしてのMnS、又は、MnSe強度は弱めに制御する。このため、低温スラブ加熱による製造方法の場合には、S及びSe含有量の合計の好ましい上限は0.025%であり、さらに好ましくは0.010%である。S及びSeは仕上げ焼鈍後に残留すると化合物を形成し、鉄損を劣化させる。そのため、仕上げ焼鈍中の純化により、S及びSeをできるだけ少なくすることが好ましい。
アルミニウム(Al)は、Nと結合して(Al、Si)Nとして析出し、インヒビターとして機能する。Alを含有させる場合、Al含有量が0.010~0.0650%の範囲内にある場合に、後述の窒化により形成されるインヒビターとしてのAlNは二次再結晶温度域を拡大し、特に高温域での二次再結晶が安定する。したがって、Al含有量は0.010~0.0650%である。Al含有量の好ましい下限は0.020%であり、さらに好ましくは0.025%である。二次再結晶の安定性の観点から、Al含有量の好ましい上限は0.040%であり、さらに好ましくは0.035%である。
窒素(N)は、Alと結合してインヒビターとして機能する。Nは製造工程の途中で窒化により含有させることが可能であるため下限は規定しない。例えば、N含有量の下限は0%超であってもよく、0.001%であってもよい。一方、Nを含有させる場合、N含有量が0.012%を超えれば、鋼板中に欠陥の一種であるブリスタが発生しやすくなる。N含有量の好ましい上限は0.010%であり、さらに好ましくは0.009%である。Nは仕上げ焼鈍工程で純化され、仕上げ焼鈍工程後には0.005%以下となる。
Nb(ニオブ)、V(バナジウム)、Mo(モリブデン)、Ta(タンタル)、W(タングステン)の合計含有量は0.050%以下であればよい。Nb群元素(Nb、V、Mo、Ta、及びWの1種以上)をインヒビターの一部として活用する場合、B8の向上効果を発揮する。一方、母材鋼板にNb群元素が過剰に残留すると、磁気特性に悪影響を及ぼすことがある。そのため、Nb、V、Mo、Ta、及びWの合計含有量は、0.050%以下であればよい。さらに、Nb群元素の合計含有量が0.030%以下(好ましくは0.003%以上、0.030%以下)であると、適切なタイミングで二次再結晶を開始させるので好ましい。また、発生する二次再結晶粒の方位が非常に好ましいものとなり、最終的に磁気特性にとって好ましい組織に制御できる。特に、Nb及びTaはその効果が強く好ましい。Nb群元素の合計含有量は下限値を設ける必要がなく、下限値が0%でもよい。この下限値は、0.003%であることが好ましい。
Cu:0~0.40%、
Bi:0~0.010%、
B:0~0.080%、
P:0~0.50%、
Ti:0~0.0150%、
Sn:0~0.10%、
Sb:0~0.10%、
Cr:0~0.30%、
Ni:0~1.0%
の少なくとも1種を含有してもよい。
これら任意元素は、公知の目的に応じて含有させればよいため、任意元素の含有量の下限値を設ける必要はなく、下限値が0%でもよい。
鋳造工程では、スラブを準備する。スラブの製造方法の一例は次のとおりである。溶鋼を製造(溶製)する。溶鋼を用いてスラブを製造する。連続鋳造法によりスラブを製造してもよい。溶鋼を用いてインゴットを製造し、インゴットを分塊圧延してスラブを製造してもよい。スラブの厚さは、特に限定されない。スラブの厚さは、たとえば、150~350mmである。スラブの厚さは、好ましくは、220~280mmである。スラブとして、厚さが10~70mmの、いわゆる薄スラブを用いてもよい。薄スラブを用いる場合、熱間圧延工程において、仕上げ圧延前の粗圧延を省略できる。
炭素(C)は、製造工程においては一次再結晶組織の制御に有効な元素であるものの、最終製品への含有量が過剰であると磁気特性に悪影響を及ぼす。したがって、C含有量は0.085%以下である。C含有量の好ましい上限は0.075%である。Cは脱炭焼鈍工程及び仕上げ焼鈍工程で純化され、0.005%以下となる。Cを含む場合、工業生産における生産性を考慮すると、C含有量の下限は0%超であってもよく、0.001%であってもよい。
シリコン(Si)は、方向性電磁鋼板の電気抵抗を高めて鉄損を低下させる。Si含有量が2.0%未満であれば、仕上げ焼鈍時にγ変態が生じて、方向性電磁鋼板の結晶方位が損なわれてしまう。一方、Si含有量が7.0%を超えれば、冷間加工性が低下して、冷間圧延時に割れが発生しやすくなる。Si含有量の好ましい下限は2.5%であり、さらに好ましくは3.0%である。Si含有量の好ましい上限は4.5%であり、さらに好ましくは4.0%である。
マンガン(Mn)はS又はSeと結合して、MnS、又は、MnSeを生成し、インヒビターとして機能する。Mnを含有させる場合、Mn含有量が0.05~1.00%の範囲内にある場合に、二次再結晶が安定する。なお、インヒビターの機能の一部をNb群元素の窒化物によって担うことが可能である。この場合は、一般的なインヒビターとしてのMnS、又は、MnSe強度は弱めに制御する。このため、Mn含有量の好ましい上限は0.50%であり、さらに好ましくは0.20%である。
硫黄(S)及びセレン(Se)は、Mnと結合して、MnS又はMnSeを生成し、インヒビターとして機能する。S及びSeの少なくとも一方を含有させる場合、S及びSeの含有量が合計で0.003~0.035%であれば、二次再結晶が安定する。なお、インヒビターの機能の一部をNb群元素の窒化物によって担うことが可能である。この場合は、一般的なインヒビターとしてのMnS、又は、MnSe強度は弱めに制御する。このため、S及びSe含有量の合計の好ましい上限は0.025%であり、さらに好ましくは0.010%である。S及びSeは仕上げ焼鈍後に残留すると化合物を形成し、鉄損を劣化させる。そのため、仕上げ焼鈍中の純化により、S及びSeをできるだけ少なくすることが好ましい。
アルミニウム(Al)は、Nと結合して(Al、Si)Nとして析出し、インヒビターとして機能する。Alを含有させる場合、Al含有量が0.010~0.065%の範囲内にある場合に、後述の窒化により形成されるインヒビターとしてのAlNは二次再結晶温度域を拡大し、特に高温域での二次再結晶が安定する。したがって、Al含有量は0.010~0.065%である。Al含有量の好ましい下限は0.020%であり、さらに好ましくは0.025%である。二次再結晶の安定性の観点から、Al含有量の好ましい上限は0.040%であり、さらに好ましくは0.035%である。
窒素(N)は、Alと結合してインヒビターとして機能する。Nは製造工程の途中で窒化により含有させることが可能であるため下限は規定しない。例えば、N含有量の下限は0%超であってもよく、0.001%であってもよい。一方、Nを含有させる場合、N含有量が0.012%を超えれば、鋼板中に欠陥の一種であるブリスタが発生しやすくなる。N含有量の好ましい上限は0.010%であり、さらに好ましくは0.009%である。Nは仕上げ焼鈍工程で純化され、仕上げ焼鈍工程後には0.005%以下となる。
Nb群元素(Nb、V、Mo、Ta、及びWの1種以上)の合計含有量は0.050%以下であればよい。Nb群元素をインヒビターの一部として活用する場合、Nb群元素の合計含有量が0.030%以下であると、適切なタイミングで二次再結晶を開始させるので好ましい。また、発生する二次再結晶粒の方位が非常に好ましいものとなり、最終的に磁気特性にとって好ましい組織に制御できる。特に、Nb及びTaはその効果が強く好ましい。Nb群元素の合計含有量は下限値を設ける必要がなく、下限値が0%でもよい。この下限値は、0.003%であることが好ましい。
Cu:0.40%以下、
Bi:0.010%以下、
B:0.080%以下、
P:0.50%以下、
Ti:0.015%以下、
Sn:0.10%以下、
Sb:0.10%以下、
Cr:0.30%以下、
Ni:1.00%以下
の少なくとも1種を含有してもよい。
これら任意元素は、公知の目的に応じて含有させればよいため、任意元素の含有量の下限値を設ける必要はなく、下限値が0%でもよい。
熱間圧延工程は、所定の温度(例えば1100~1400℃)に加熱されたスラブの熱間圧延を行い、熱延鋼板を得る工程である。熱間圧延工程では、例えば、加熱工程で加熱された珪素鋼素材(スラブ)の粗圧延を行った後、仕上げ圧延を行って所定厚さ、例えば、1.8~3.5mmの熱延鋼板とする。仕上げ圧延終了後、熱延鋼板を所定の温度で巻き取る。
熱延板焼鈍工程は、熱間圧延工程で得た熱延鋼板を所定の温度条件(例えば750~1200℃で30秒間~10分間)で焼鈍して、焼鈍鋼板を得る工程である。熱延板焼鈍は、一般的に、熱間圧延工程後の熱延鋼板を焼鈍することにより、再結晶率や残存歪や結晶粒径などの鋼板組織を制御し、また鋼中の析出物形態を好ましく調整するために実施される。例えば、高温スラブ加熱プロセスにおいては、AlNなどの析出物の形態を最終的に制御する工程であり、均一かつ微細に析出するように条件調整する。熱延板焼鈍として、例えば、鋼板を1050℃~1150℃に加熱した後、AlNなどを適正に析出させるため、50~150秒かけて中間温度(850℃~950℃)まで緩冷却した後、水冷却してもよい。
冷間圧延工程は、熱延板焼鈍工程で得た焼鈍鋼板を、1回の冷間圧延、又は焼鈍(中間焼鈍)を介して複数回(2回以上)の冷間圧延(例えば総冷延率で80~95%)により、例えば、0.10~0.50mmの厚さを有する冷延鋼板を得る工程である。磁気特性を改善するために、例えば、冷間圧延のパス間温度を100℃~300℃程度にしてもよい。
総冷延率(%)=(1-冷間圧延後の鋼板の板厚/冷間圧延前の鋼板の板厚)×100
本実施形態では、冷間圧延工程後の冷延鋼板に対して、局所加熱領域を形成するための局所急速加熱を行う。急速加熱方法としては、鋼板を局所的に加熱できるものであればよく、特に限定しない。例えば、鋼板の表裏面にスポット電極を接触させて鋼板内に電流を通電して加熱する方式、レーザー光や電子ビームなどを鋼板表面に照射して加熱する方法、誘導加熱によって局所的に加熱する方法、熱片を接触させて加熱する方法などを採用することができる。個々の局所加熱領域の大きさとしては、直径が10μm~10mm程度の点状領域、あるいは幅が10μm~10mm程度の線状領域とすることができる。また、通電加熱に用いる電極は、上記のように円形状の電極としてもよく、または線状の電極としてもよい。
脱炭焼鈍工程では、局所急速加熱工程後の冷延鋼板に対して、脱炭焼鈍(一次焼鈍)を行う。この脱炭焼鈍により、局所加熱領域に形成されるゴス方位粒の存在頻度が増大し、ゴス方位粒の粒径が増大し、理想ゴス方位に近い方位を持つ粗大ゴス方位粒が好ましく粒成長する。脱炭焼鈍条件としては、例えば、焼鈍温度を700~900℃、焼鈍時間を1~3分間の焼鈍とすればよい。冷延鋼板に脱炭焼鈍を行うことで、冷延鋼板中に含まれるCが除去される。脱炭焼鈍は、冷延鋼板中に含まれる「C」を除去するために、湿潤雰囲気中で行うことが好ましい。
窒化処理は、スラブ加熱温度が1280℃以下の低温スラブ加熱プロセスで有効な処理であり、二次再結晶におけるインヒビターの強度を調整するために重要な工程である。窒化処理は、脱炭処理の開始から、仕上げ焼鈍における二次再結晶の開始までの間に、鋼板の窒素量を40~200ppm程度増加させる。窒化処理としては、例えば、アンモニア等の窒化能のあるガスを含有する雰囲気中で焼鈍する処理、MnN等の窒化能を有する粉末を含む焼鈍分離剤を塗布した脱炭焼鈍鋼板を仕上げ焼鈍する処理等が例示される。窒化処理後の窒化量は130~350ppmとすることが好ましく、さらには150~250ppmとすることが好ましい。
焼鈍分離剤塗布工程は、脱炭焼鈍鋼板に焼鈍分離剤を塗布する工程である。焼鈍分離剤としては、例えば、MgOを主成分とする焼鈍分離剤を用いることができる。焼鈍分離剤を塗布後の脱炭焼鈍鋼板は、コイル状に巻取った状態で、次の仕上げ焼鈍工程で仕上げ焼鈍される。
仕上げ焼鈍工程は、焼鈍分離剤が塗布された脱炭焼鈍鋼板に仕上げ焼鈍(二次焼鈍)を施し、二次再結晶を生じさせる工程である。この工程は、一次再結晶粒の成長をインヒビターにより抑制した状態で二次再結晶を進行させることによって、{100}<001>方位粒を優先成長させ、磁束密度を飛躍的に向上させる。
鋼板に、りん酸あるいはりん酸塩、無水クロム酸あるいはクロム酸塩およびコロイド状シリカを含むコーティング溶液を塗布して焼き付けて(例えば、350℃~1150℃で5~300秒間)、絶縁被膜を形成する。
方向性電磁鋼板には、必要に応じて、レーザー、プラズマ、機械的方法、エッチングなど、公知の手法により、局所的な微小歪領域または溝を形成する磁区細分化処理を施してもよい。ただ、本実施形態に係る冷延鋼板を用いて製造された方向性電磁鋼板は、優れた磁束密度を有するにもかかわらず、二次再結晶粒径の粗大化が抑制されているので、磁区細分化処理を行わなくても磁区が細分化されている。
通常 :1000℃~1200℃を15℃/時間で昇温
徐加熱1:1000℃~1200℃を10℃/時間で昇温
徐加熱 :1000℃~1200℃を7.5℃/時間で昇温
徐加熱2:1000℃~1200℃を5.0℃/時間で昇温
Step:1070℃×10時間の保定
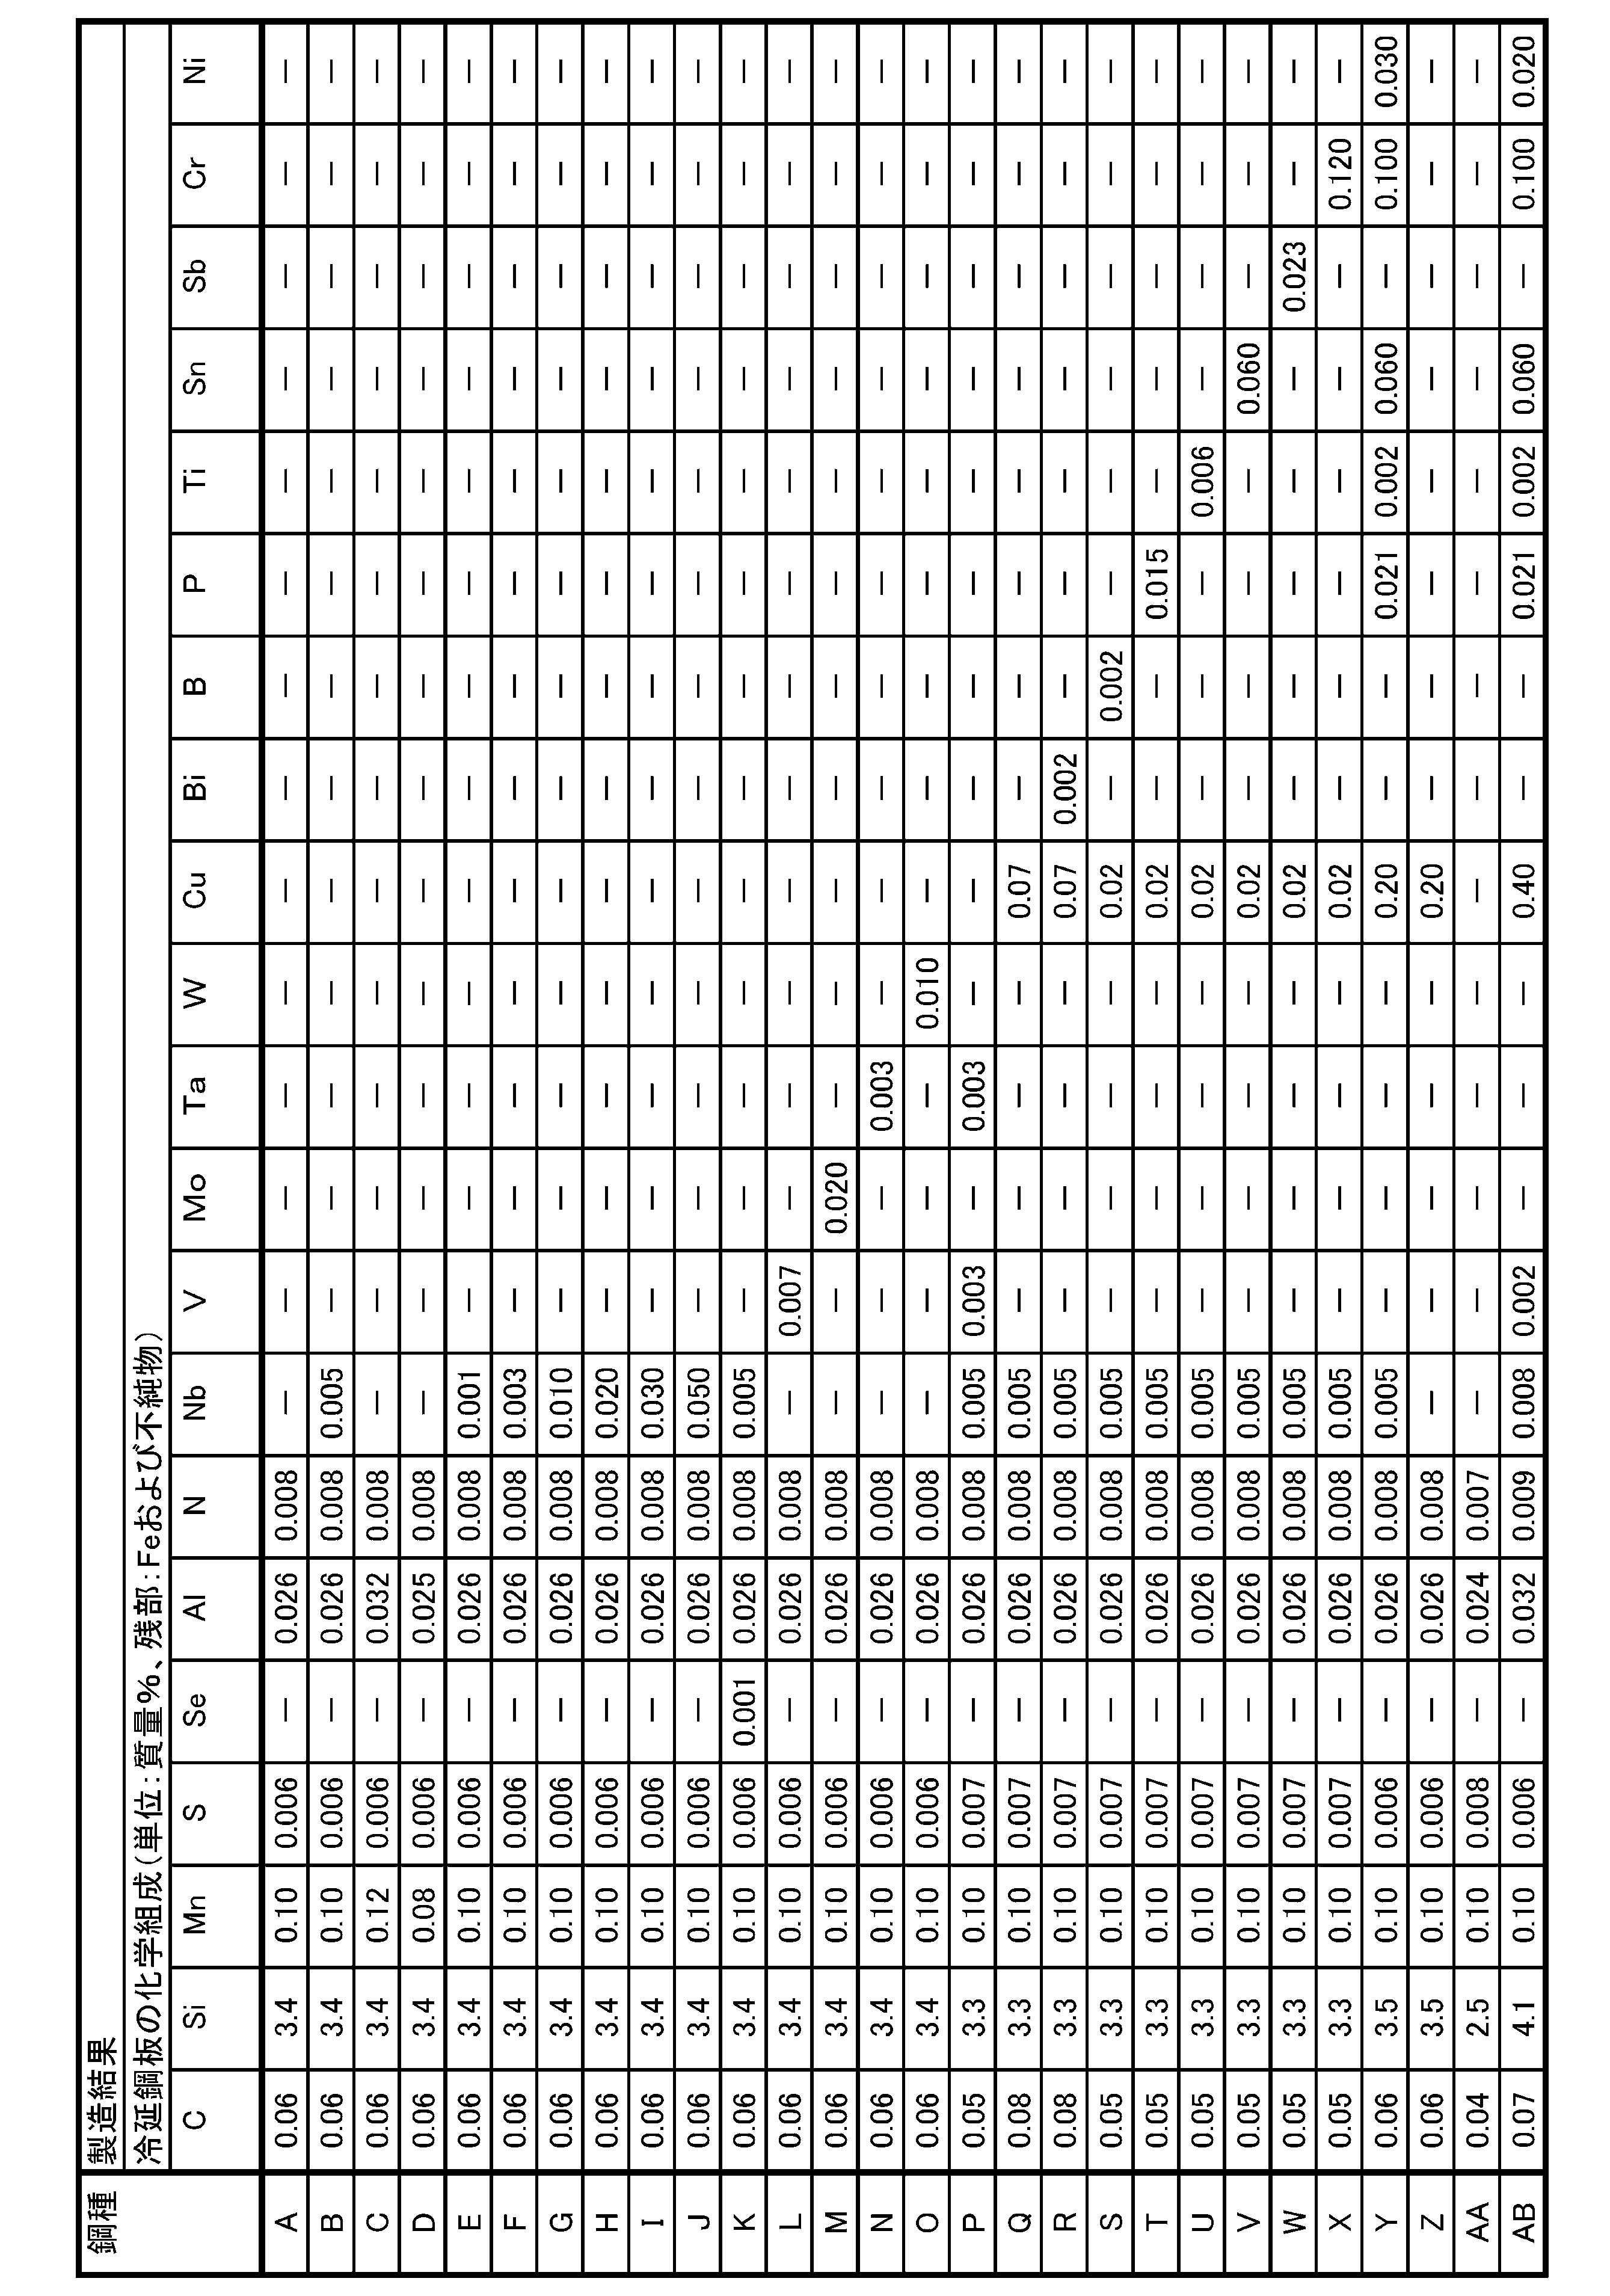
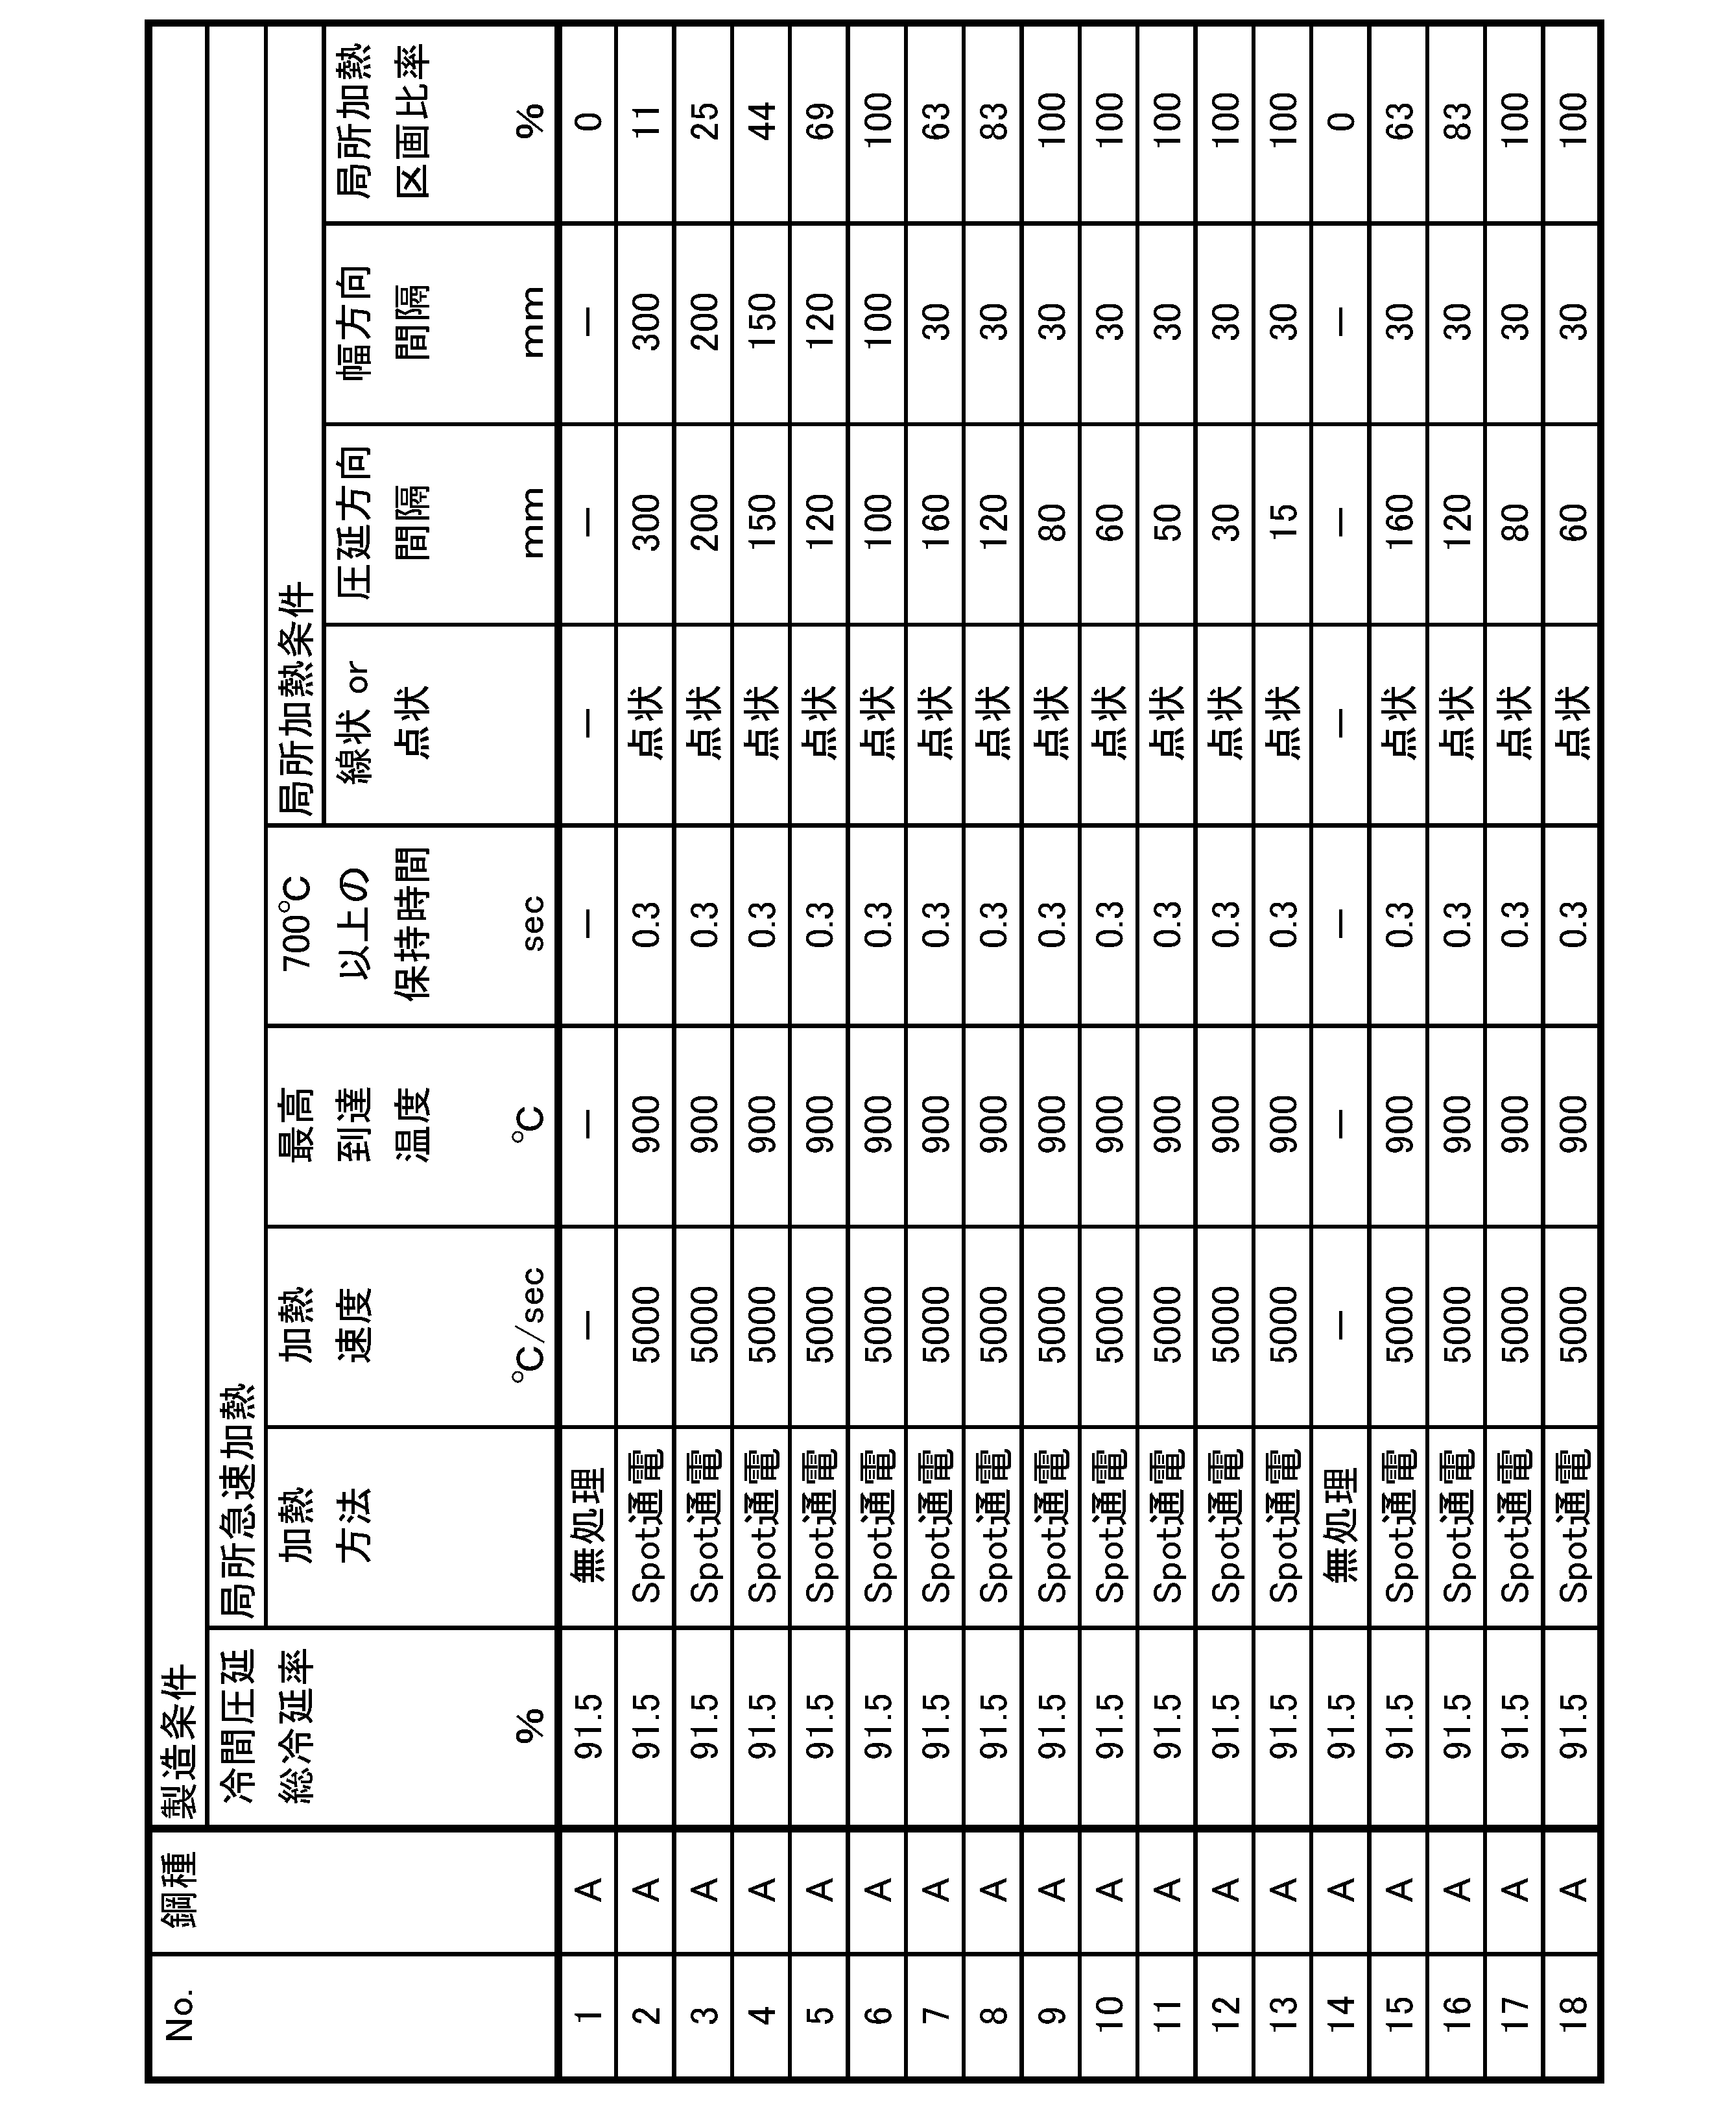
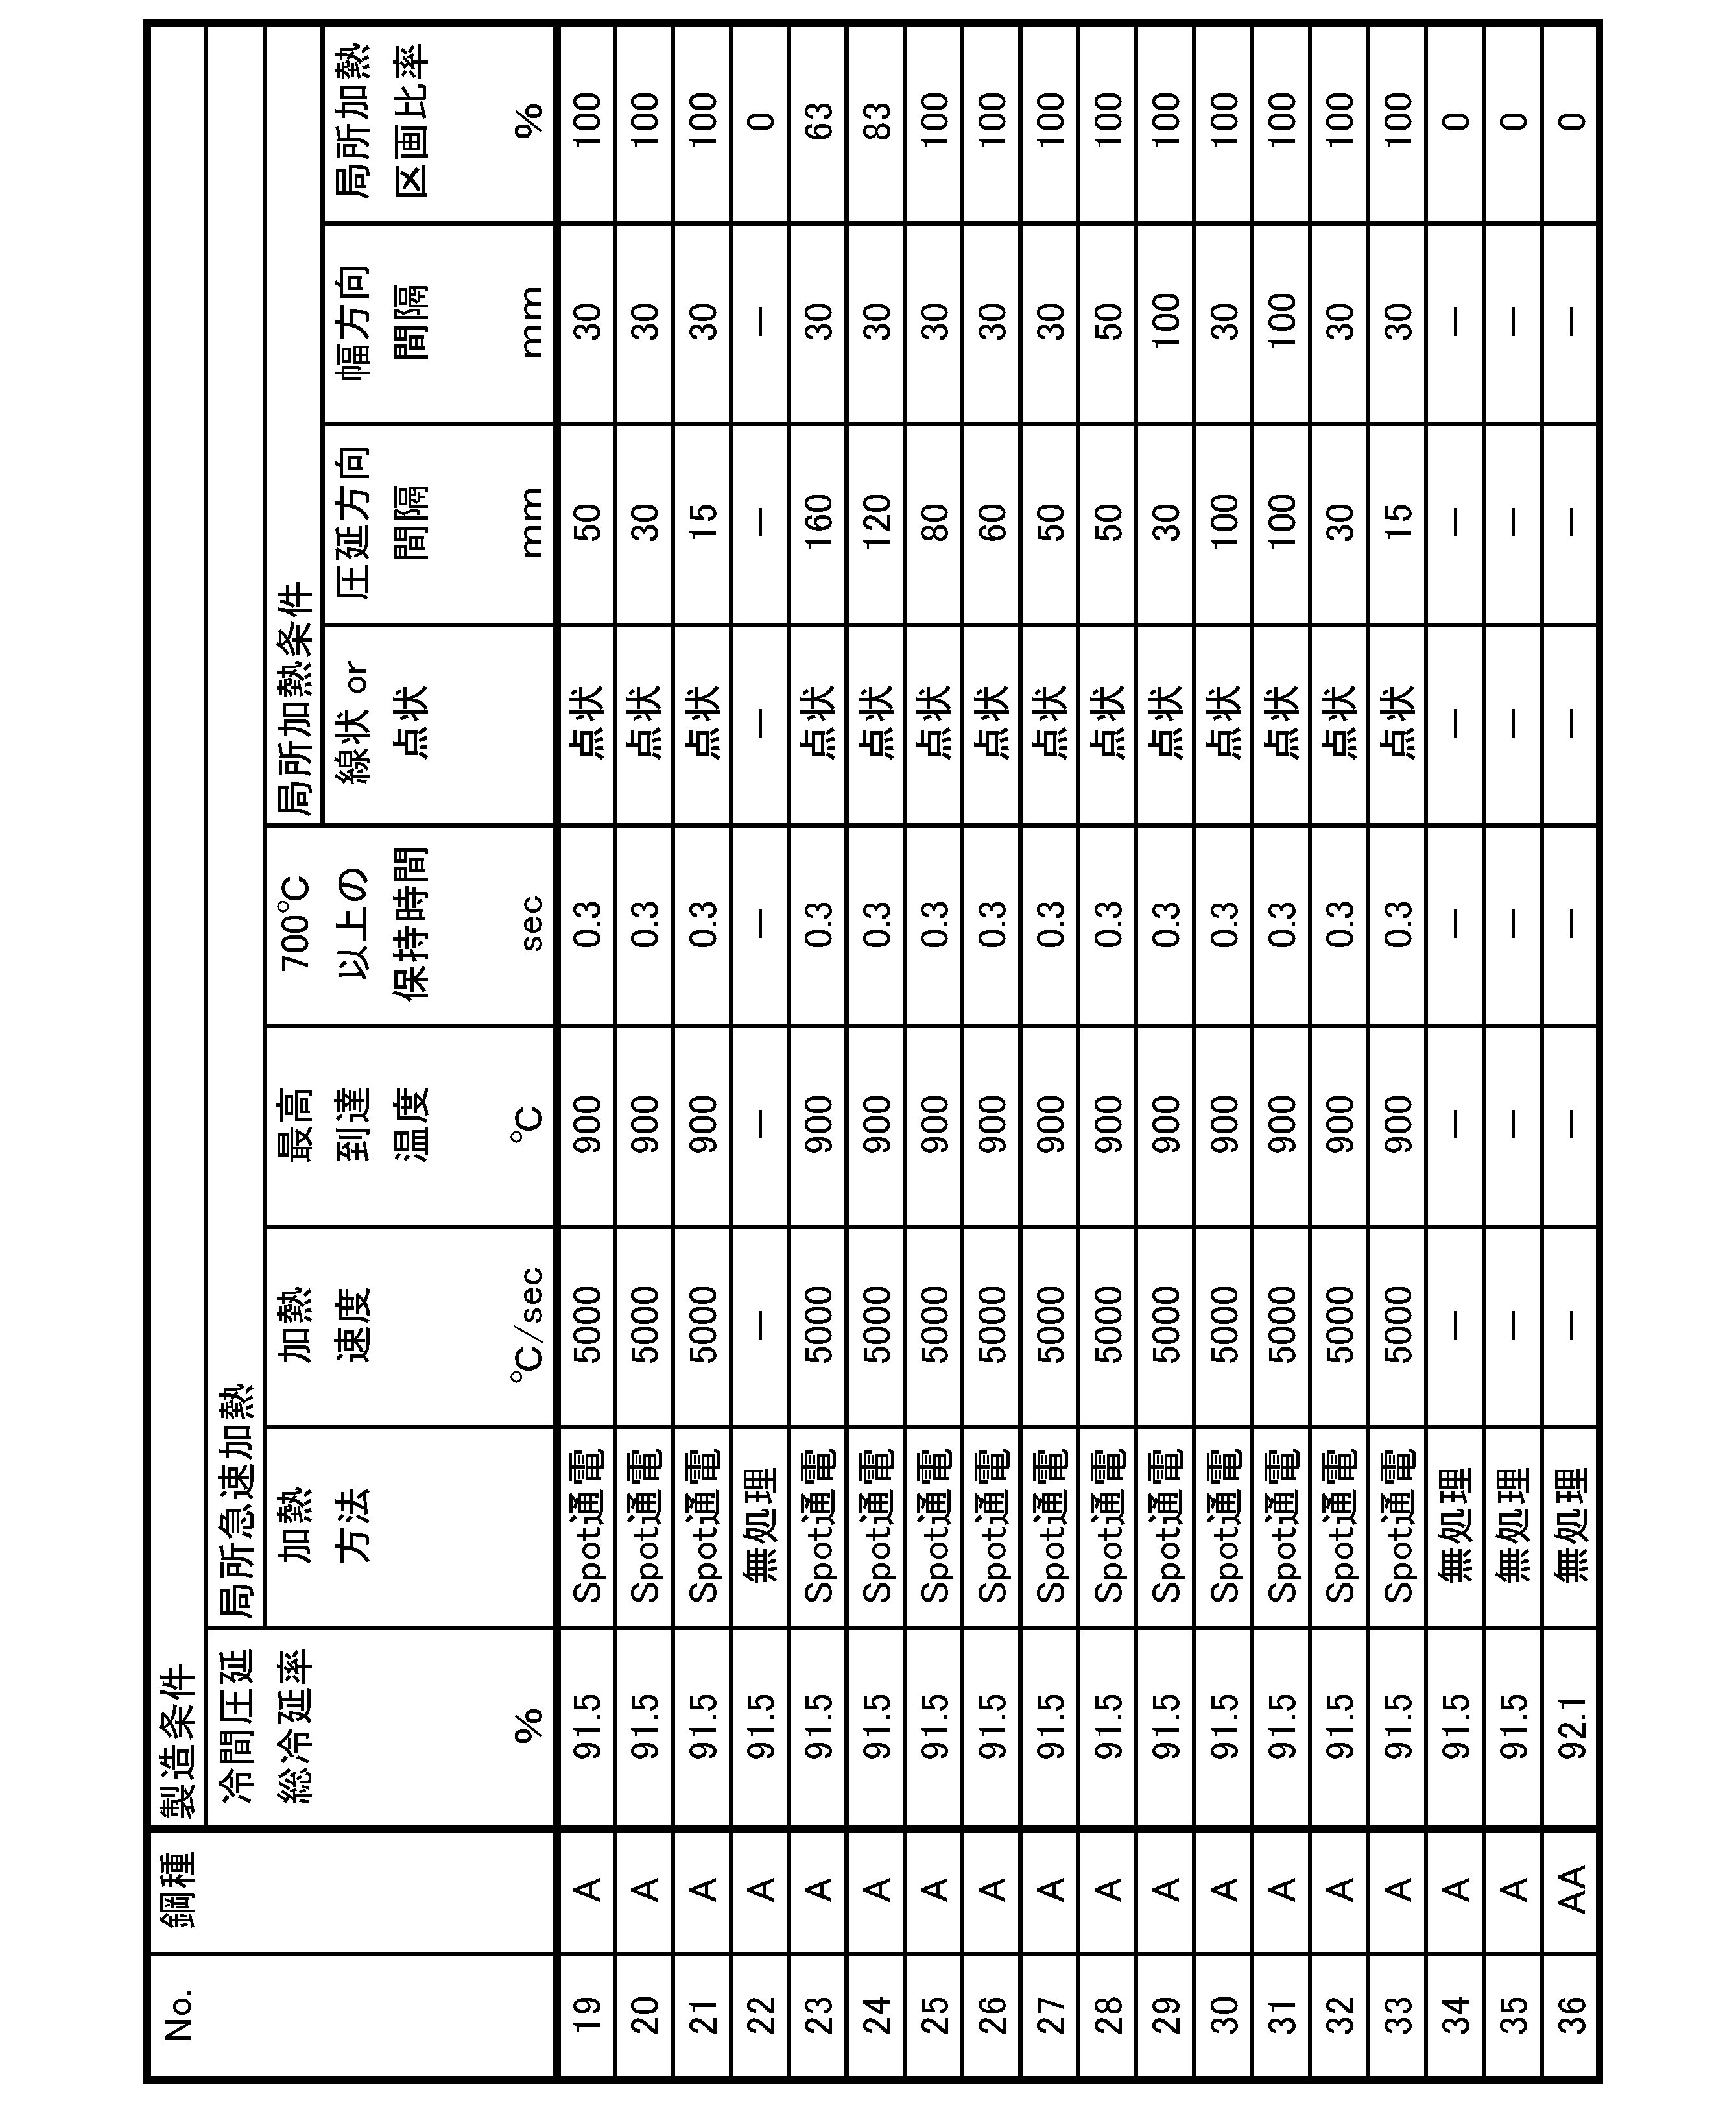
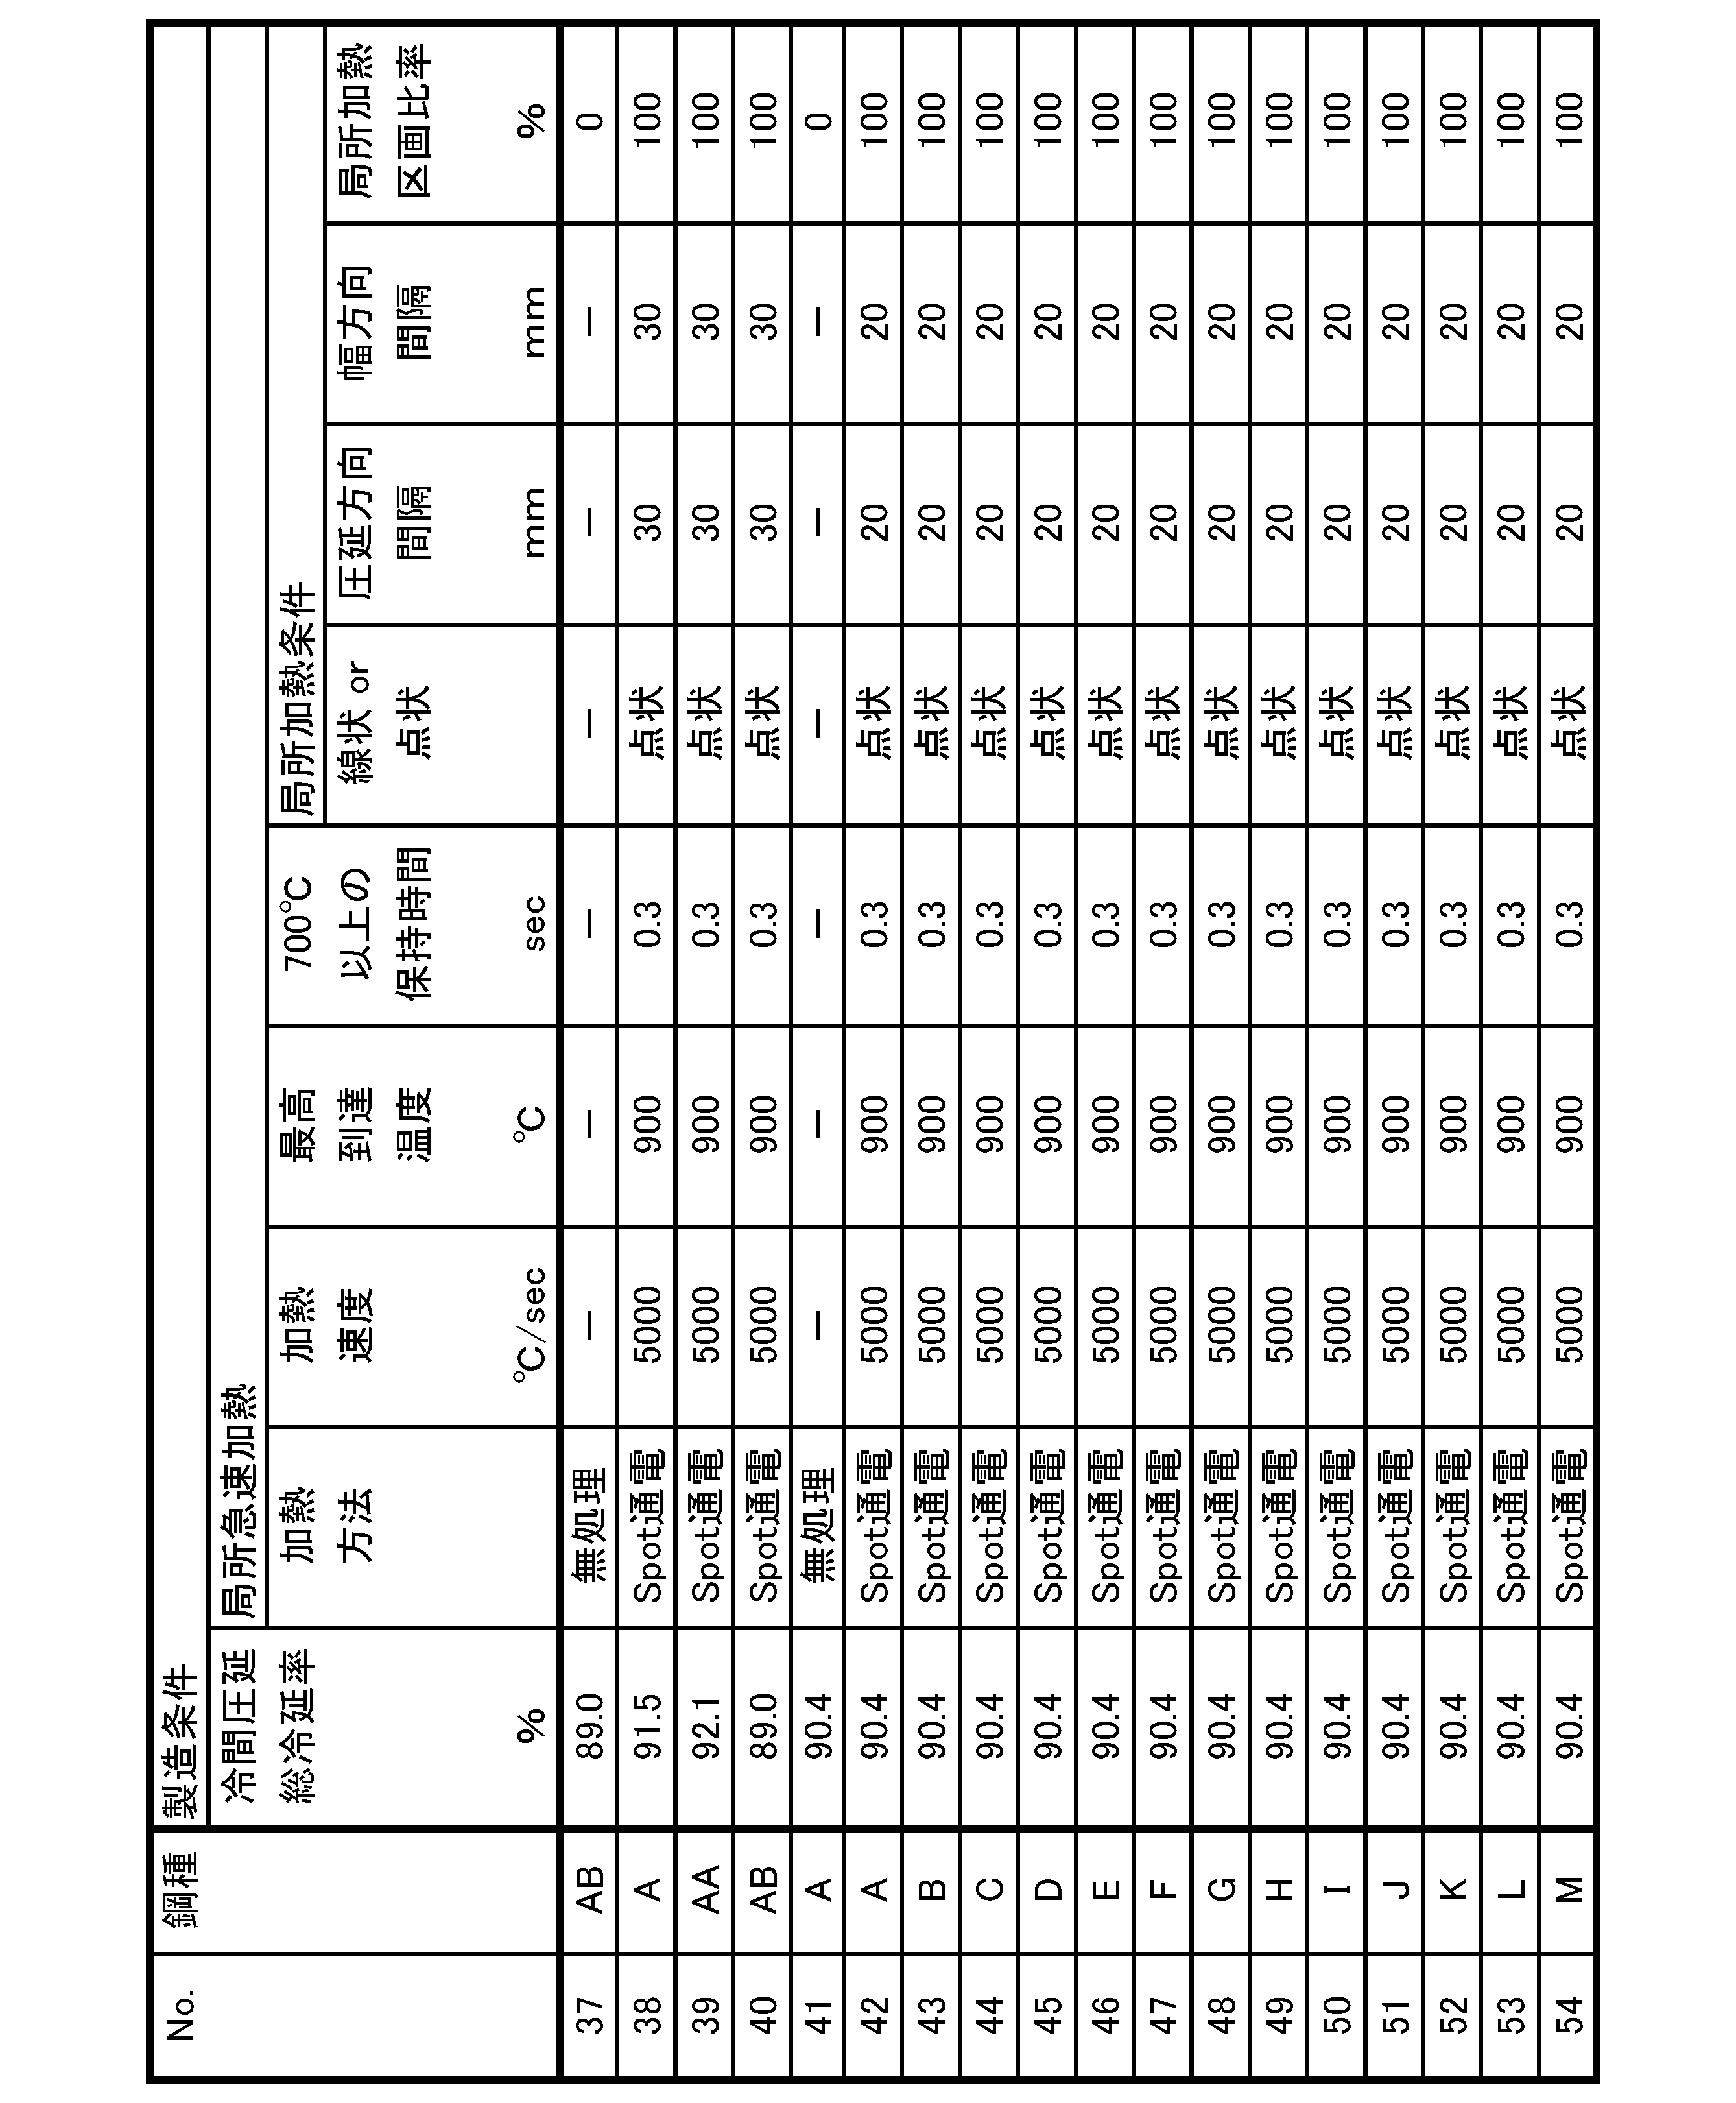
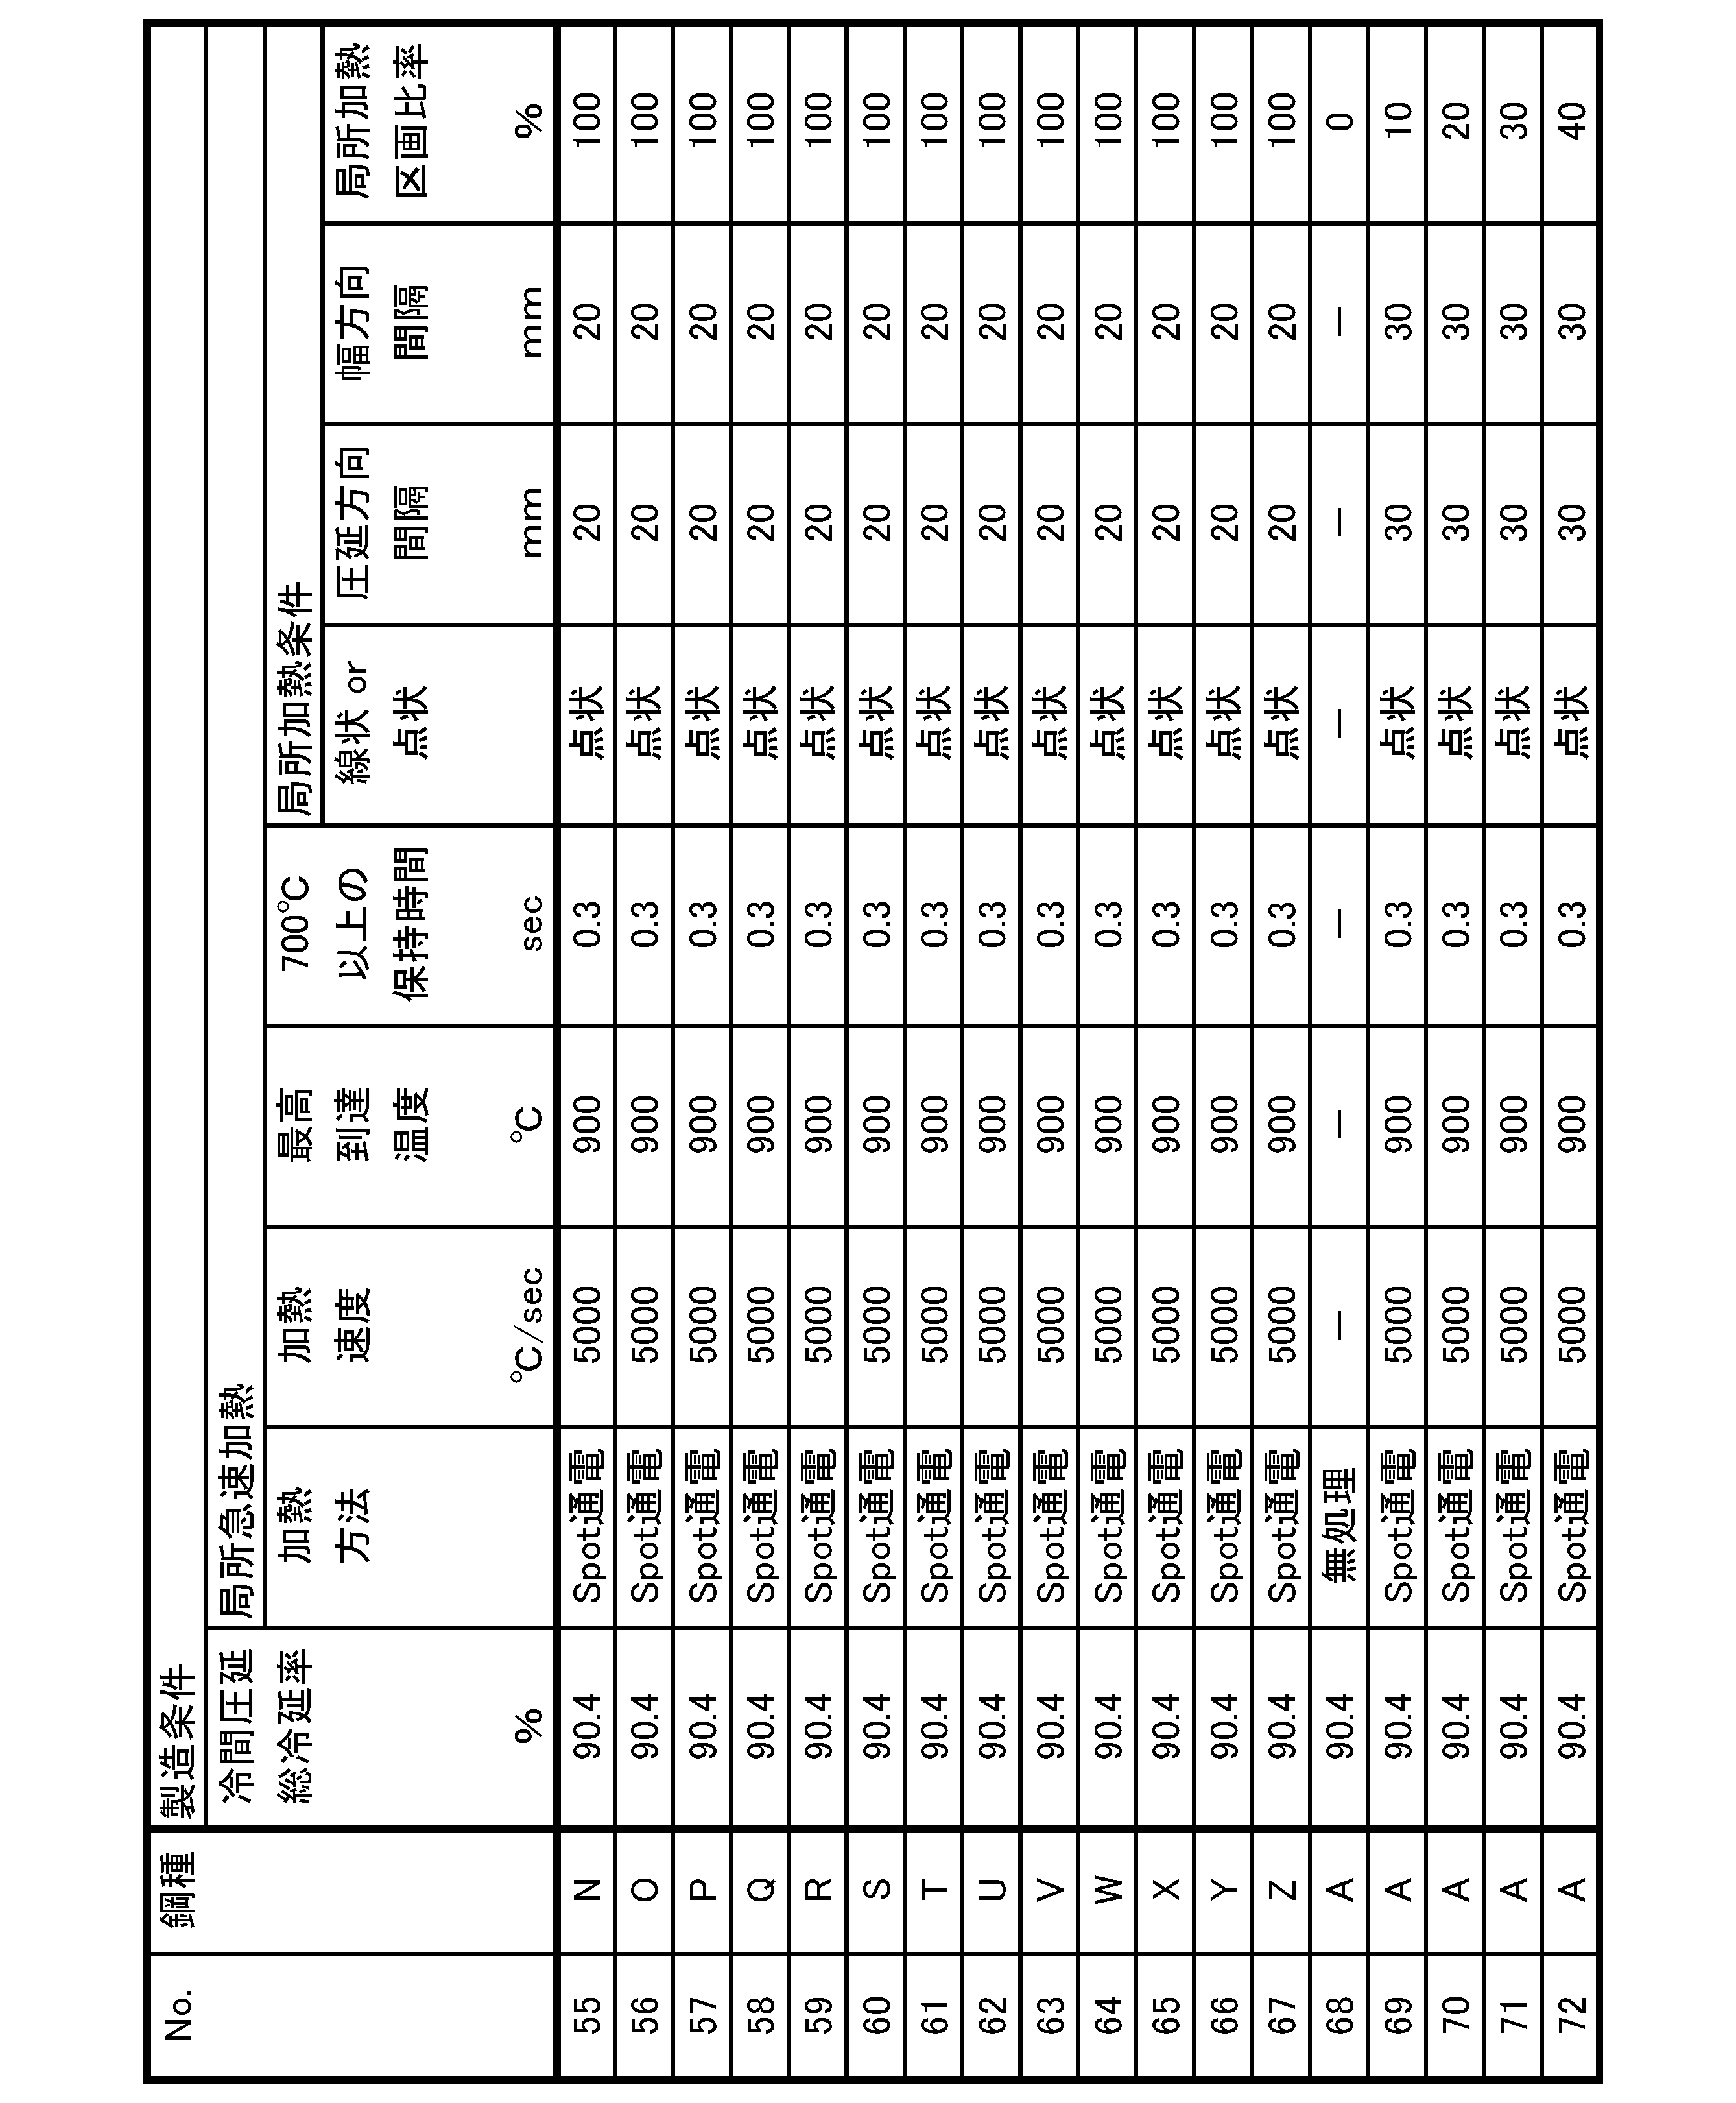
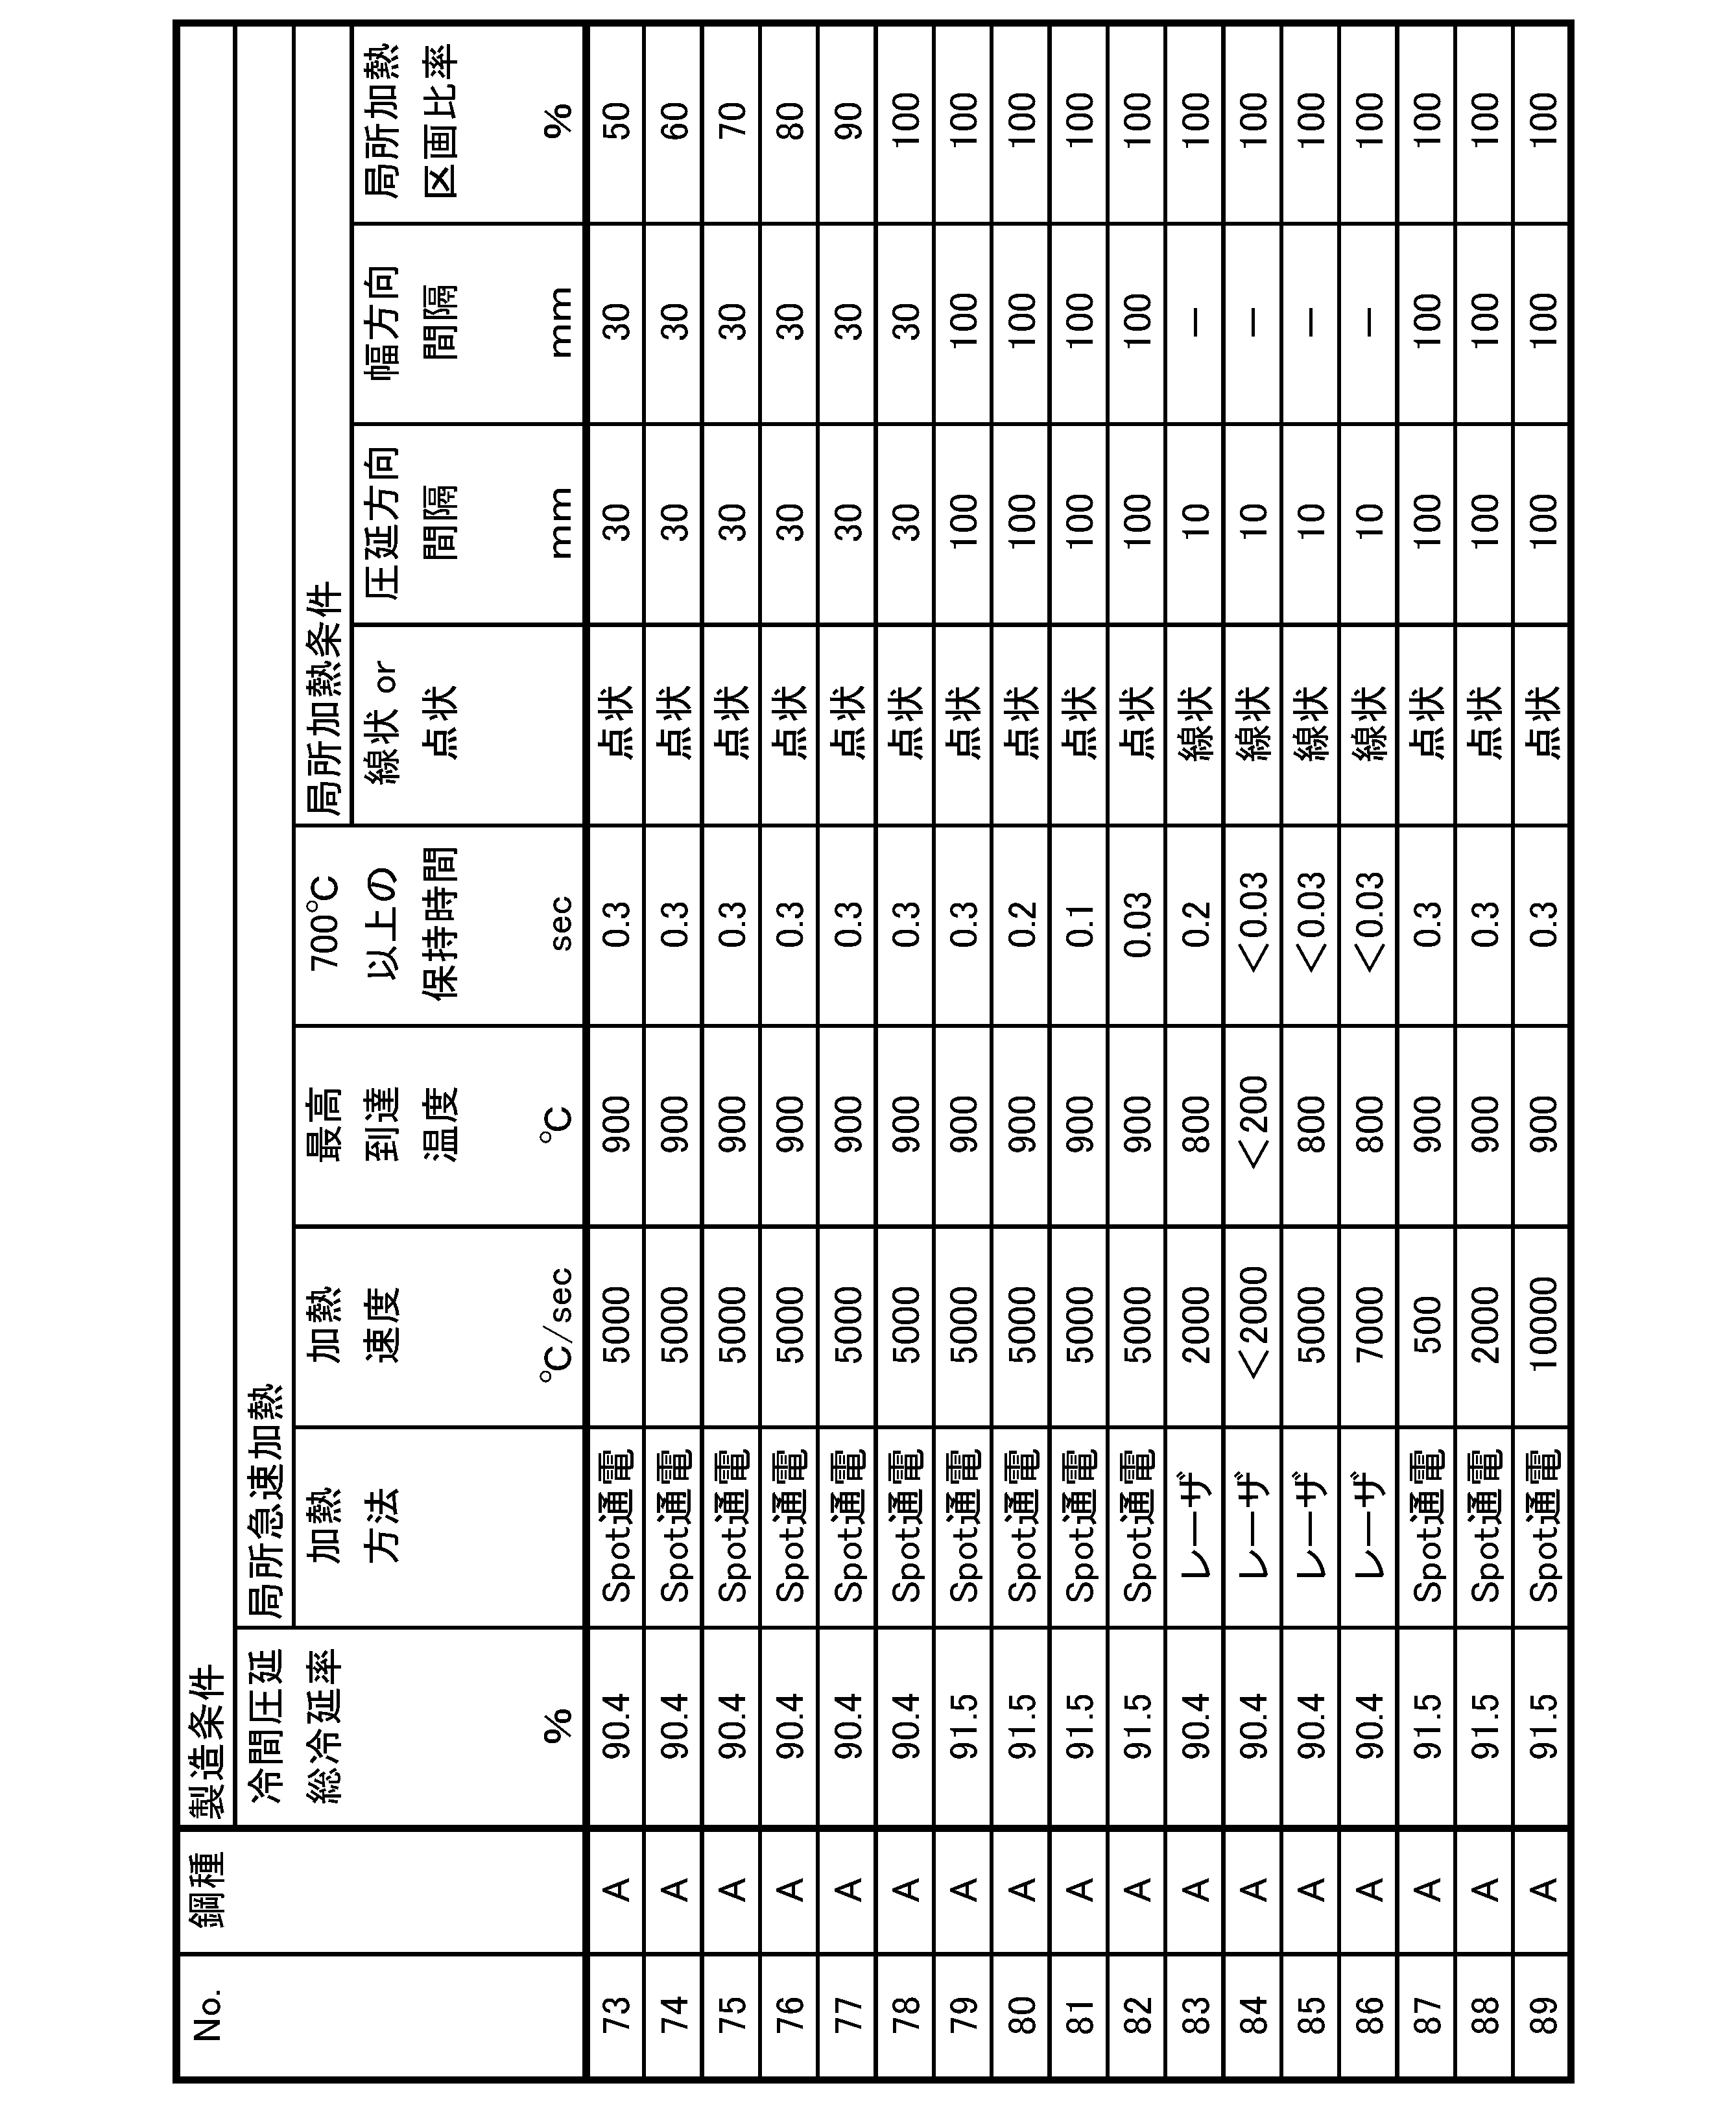
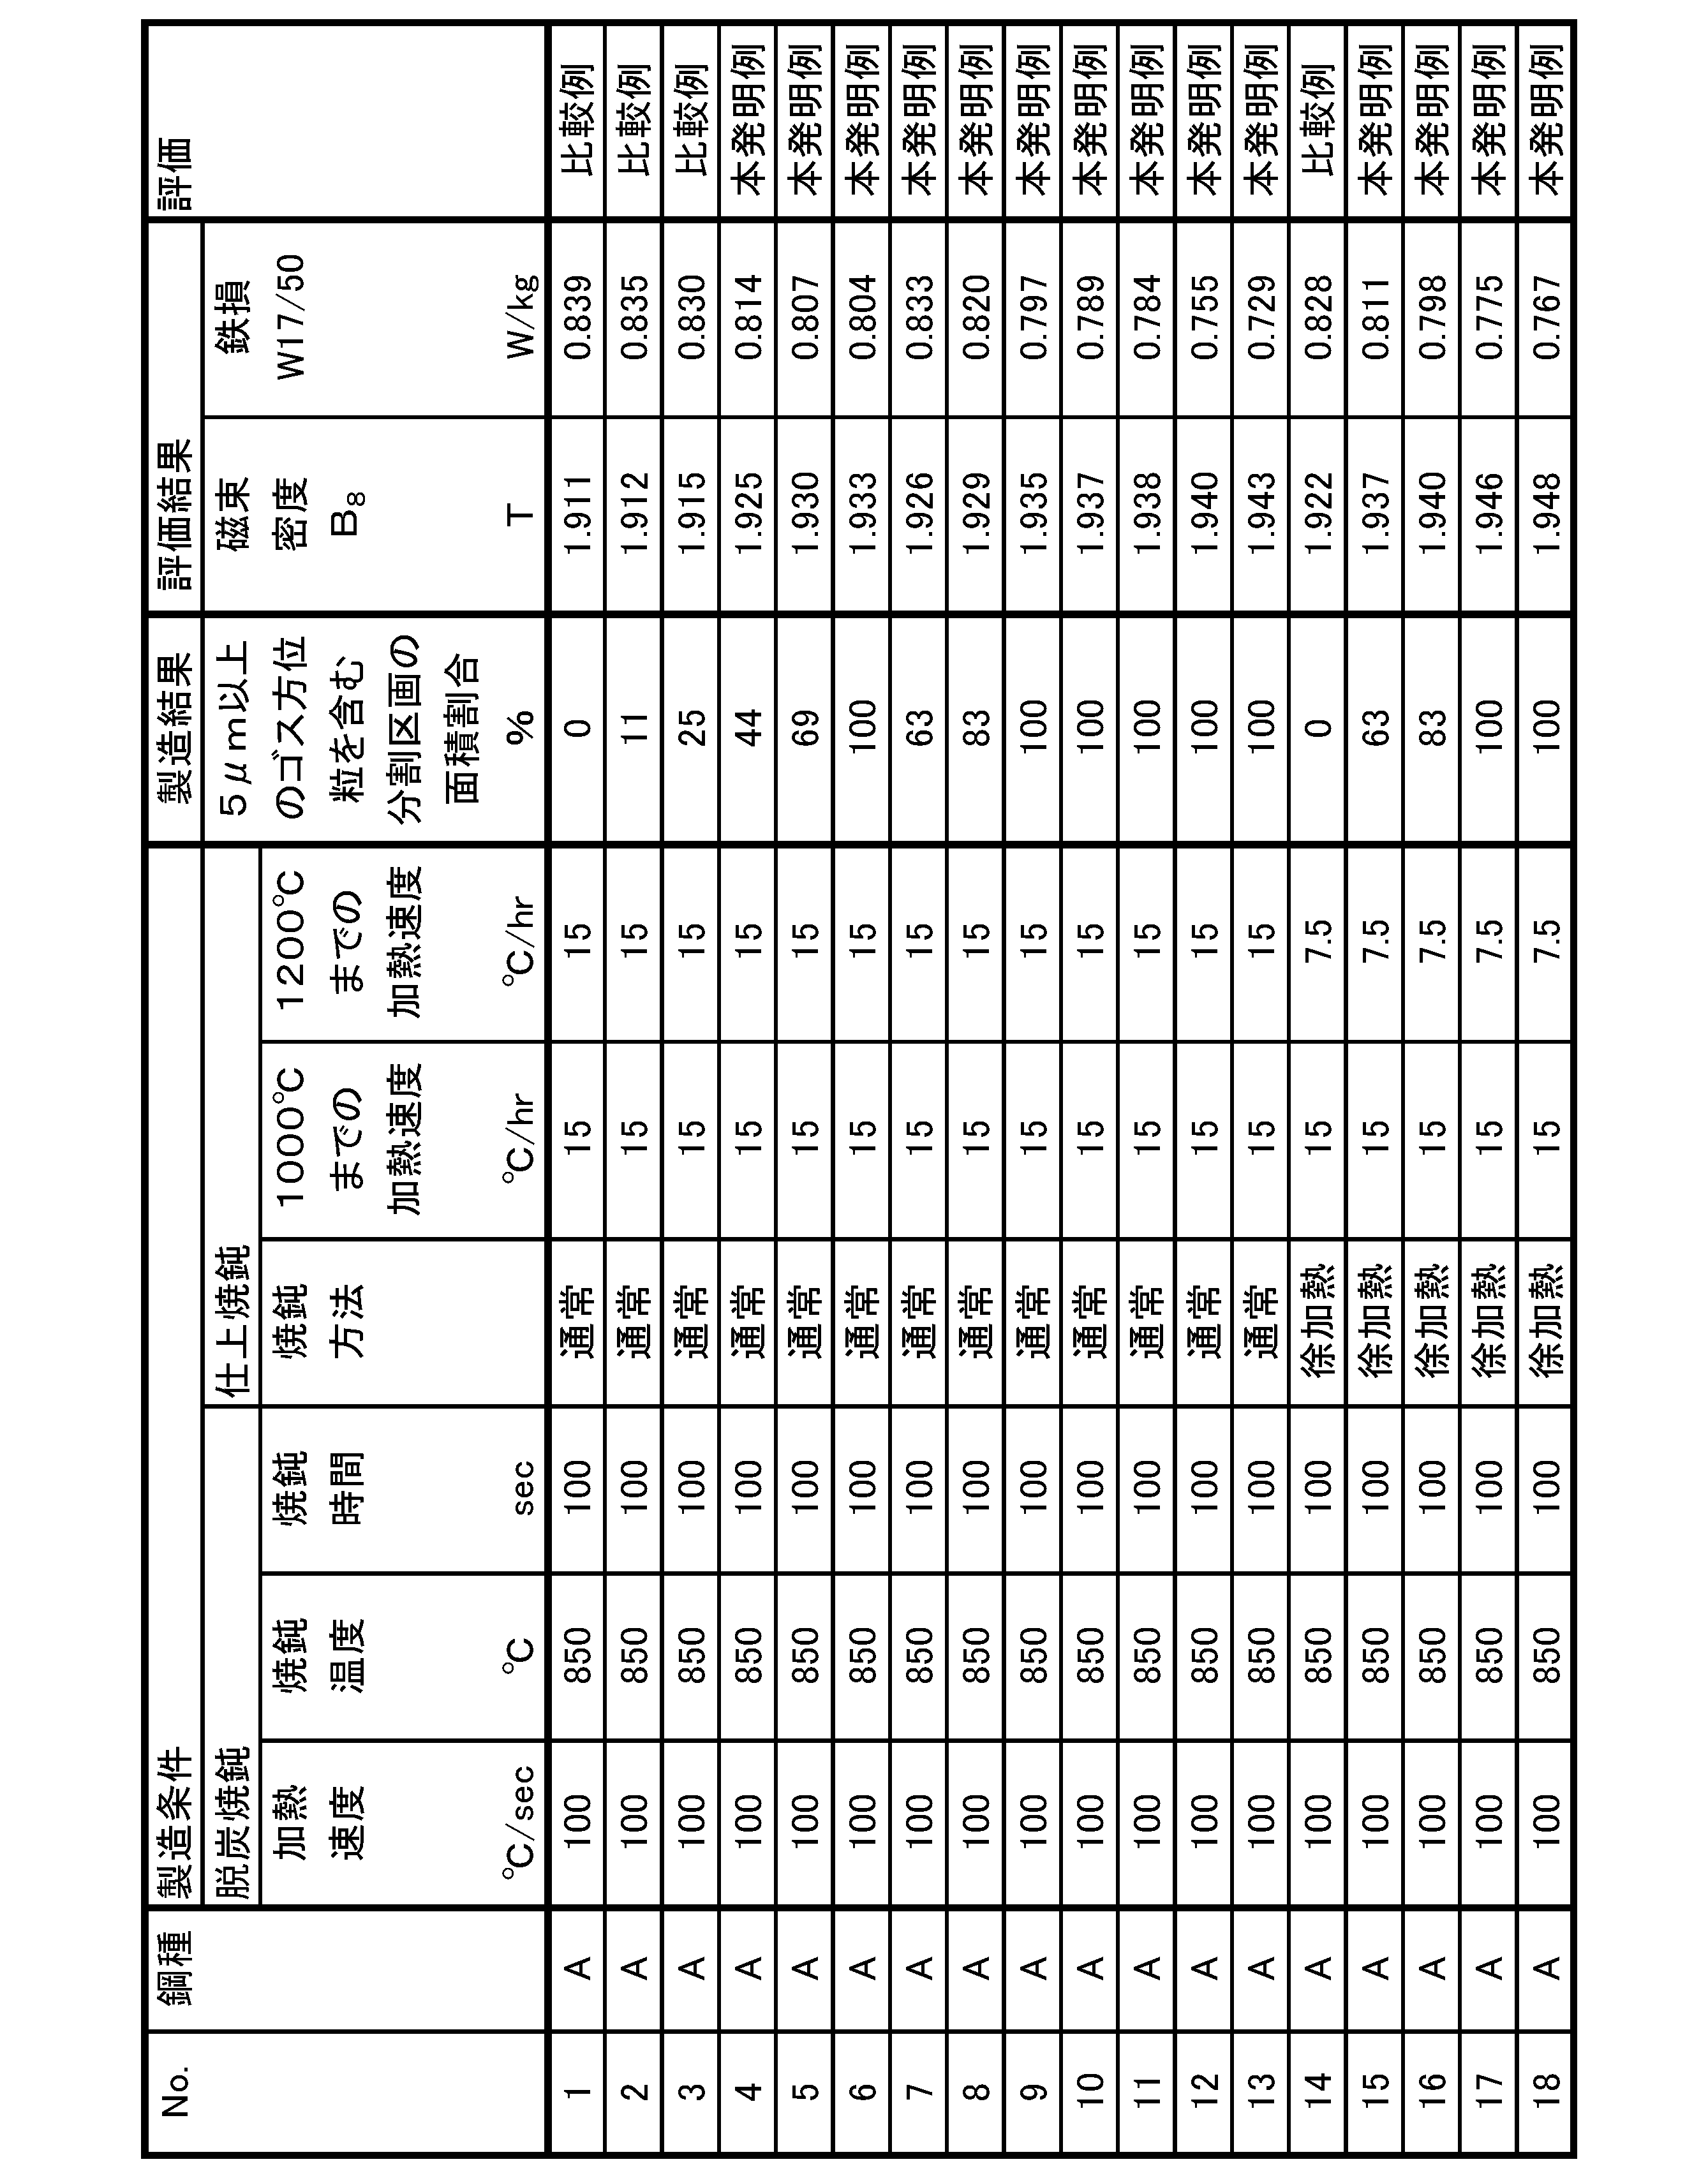
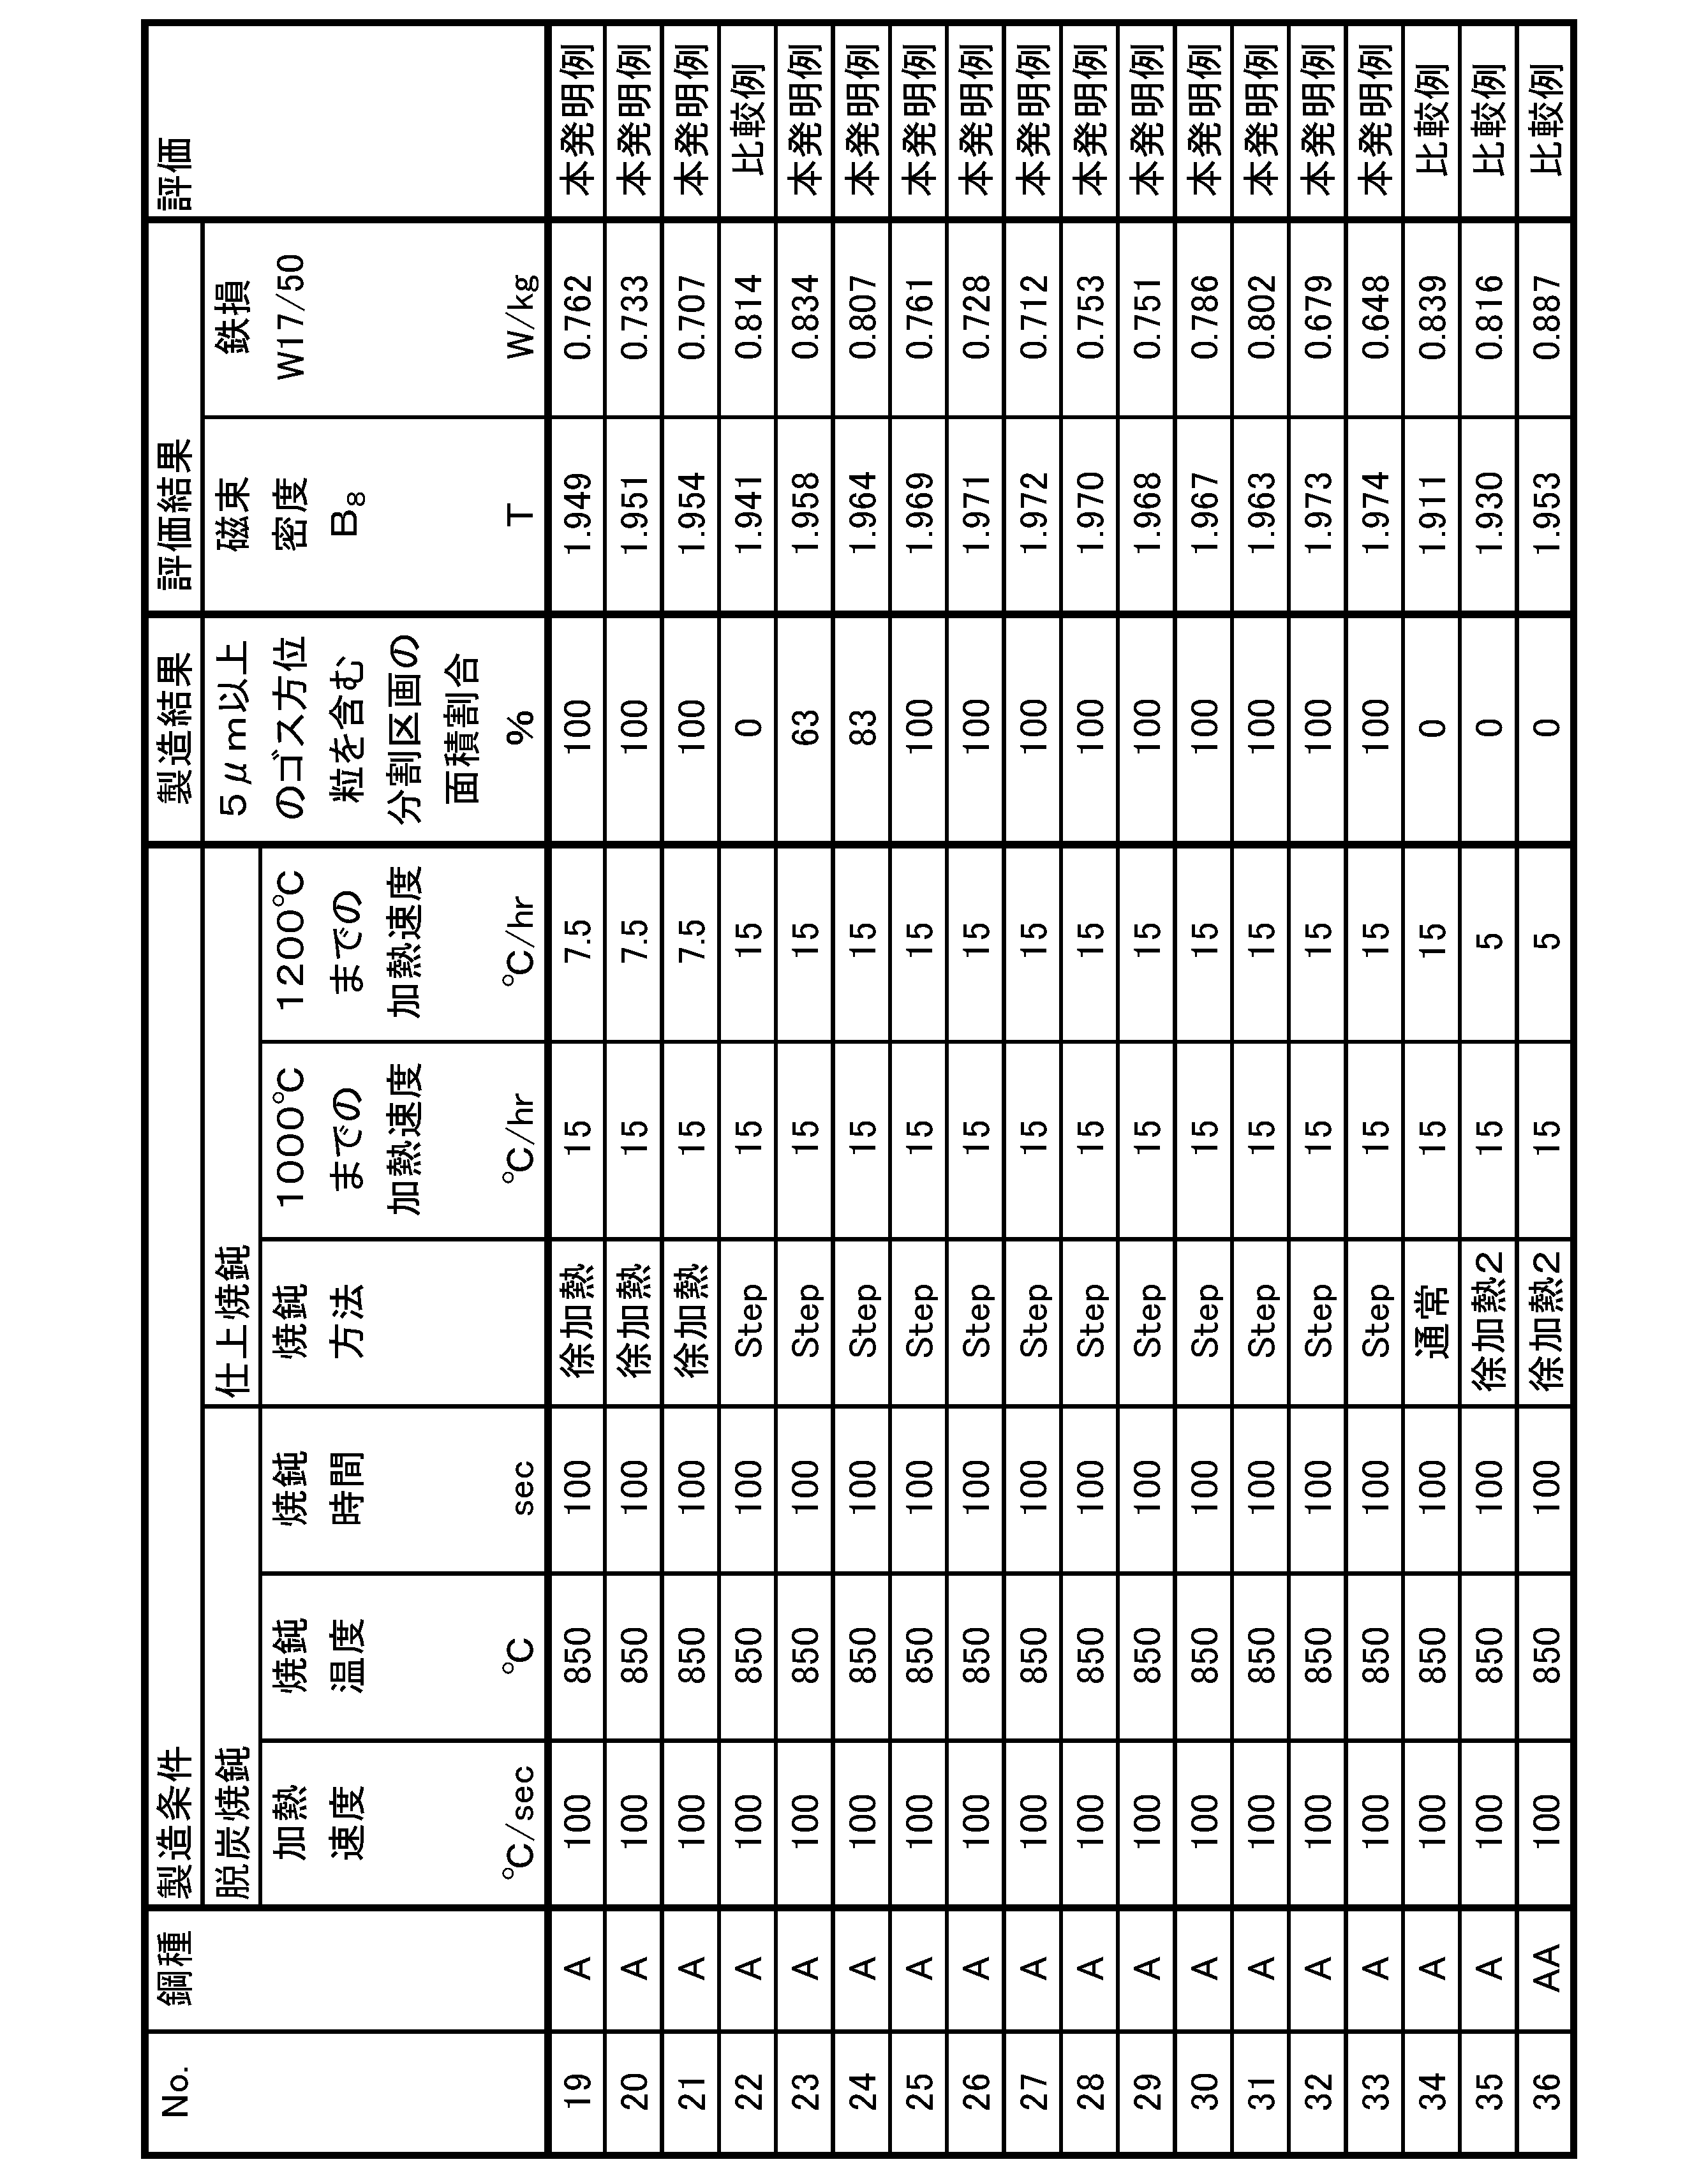
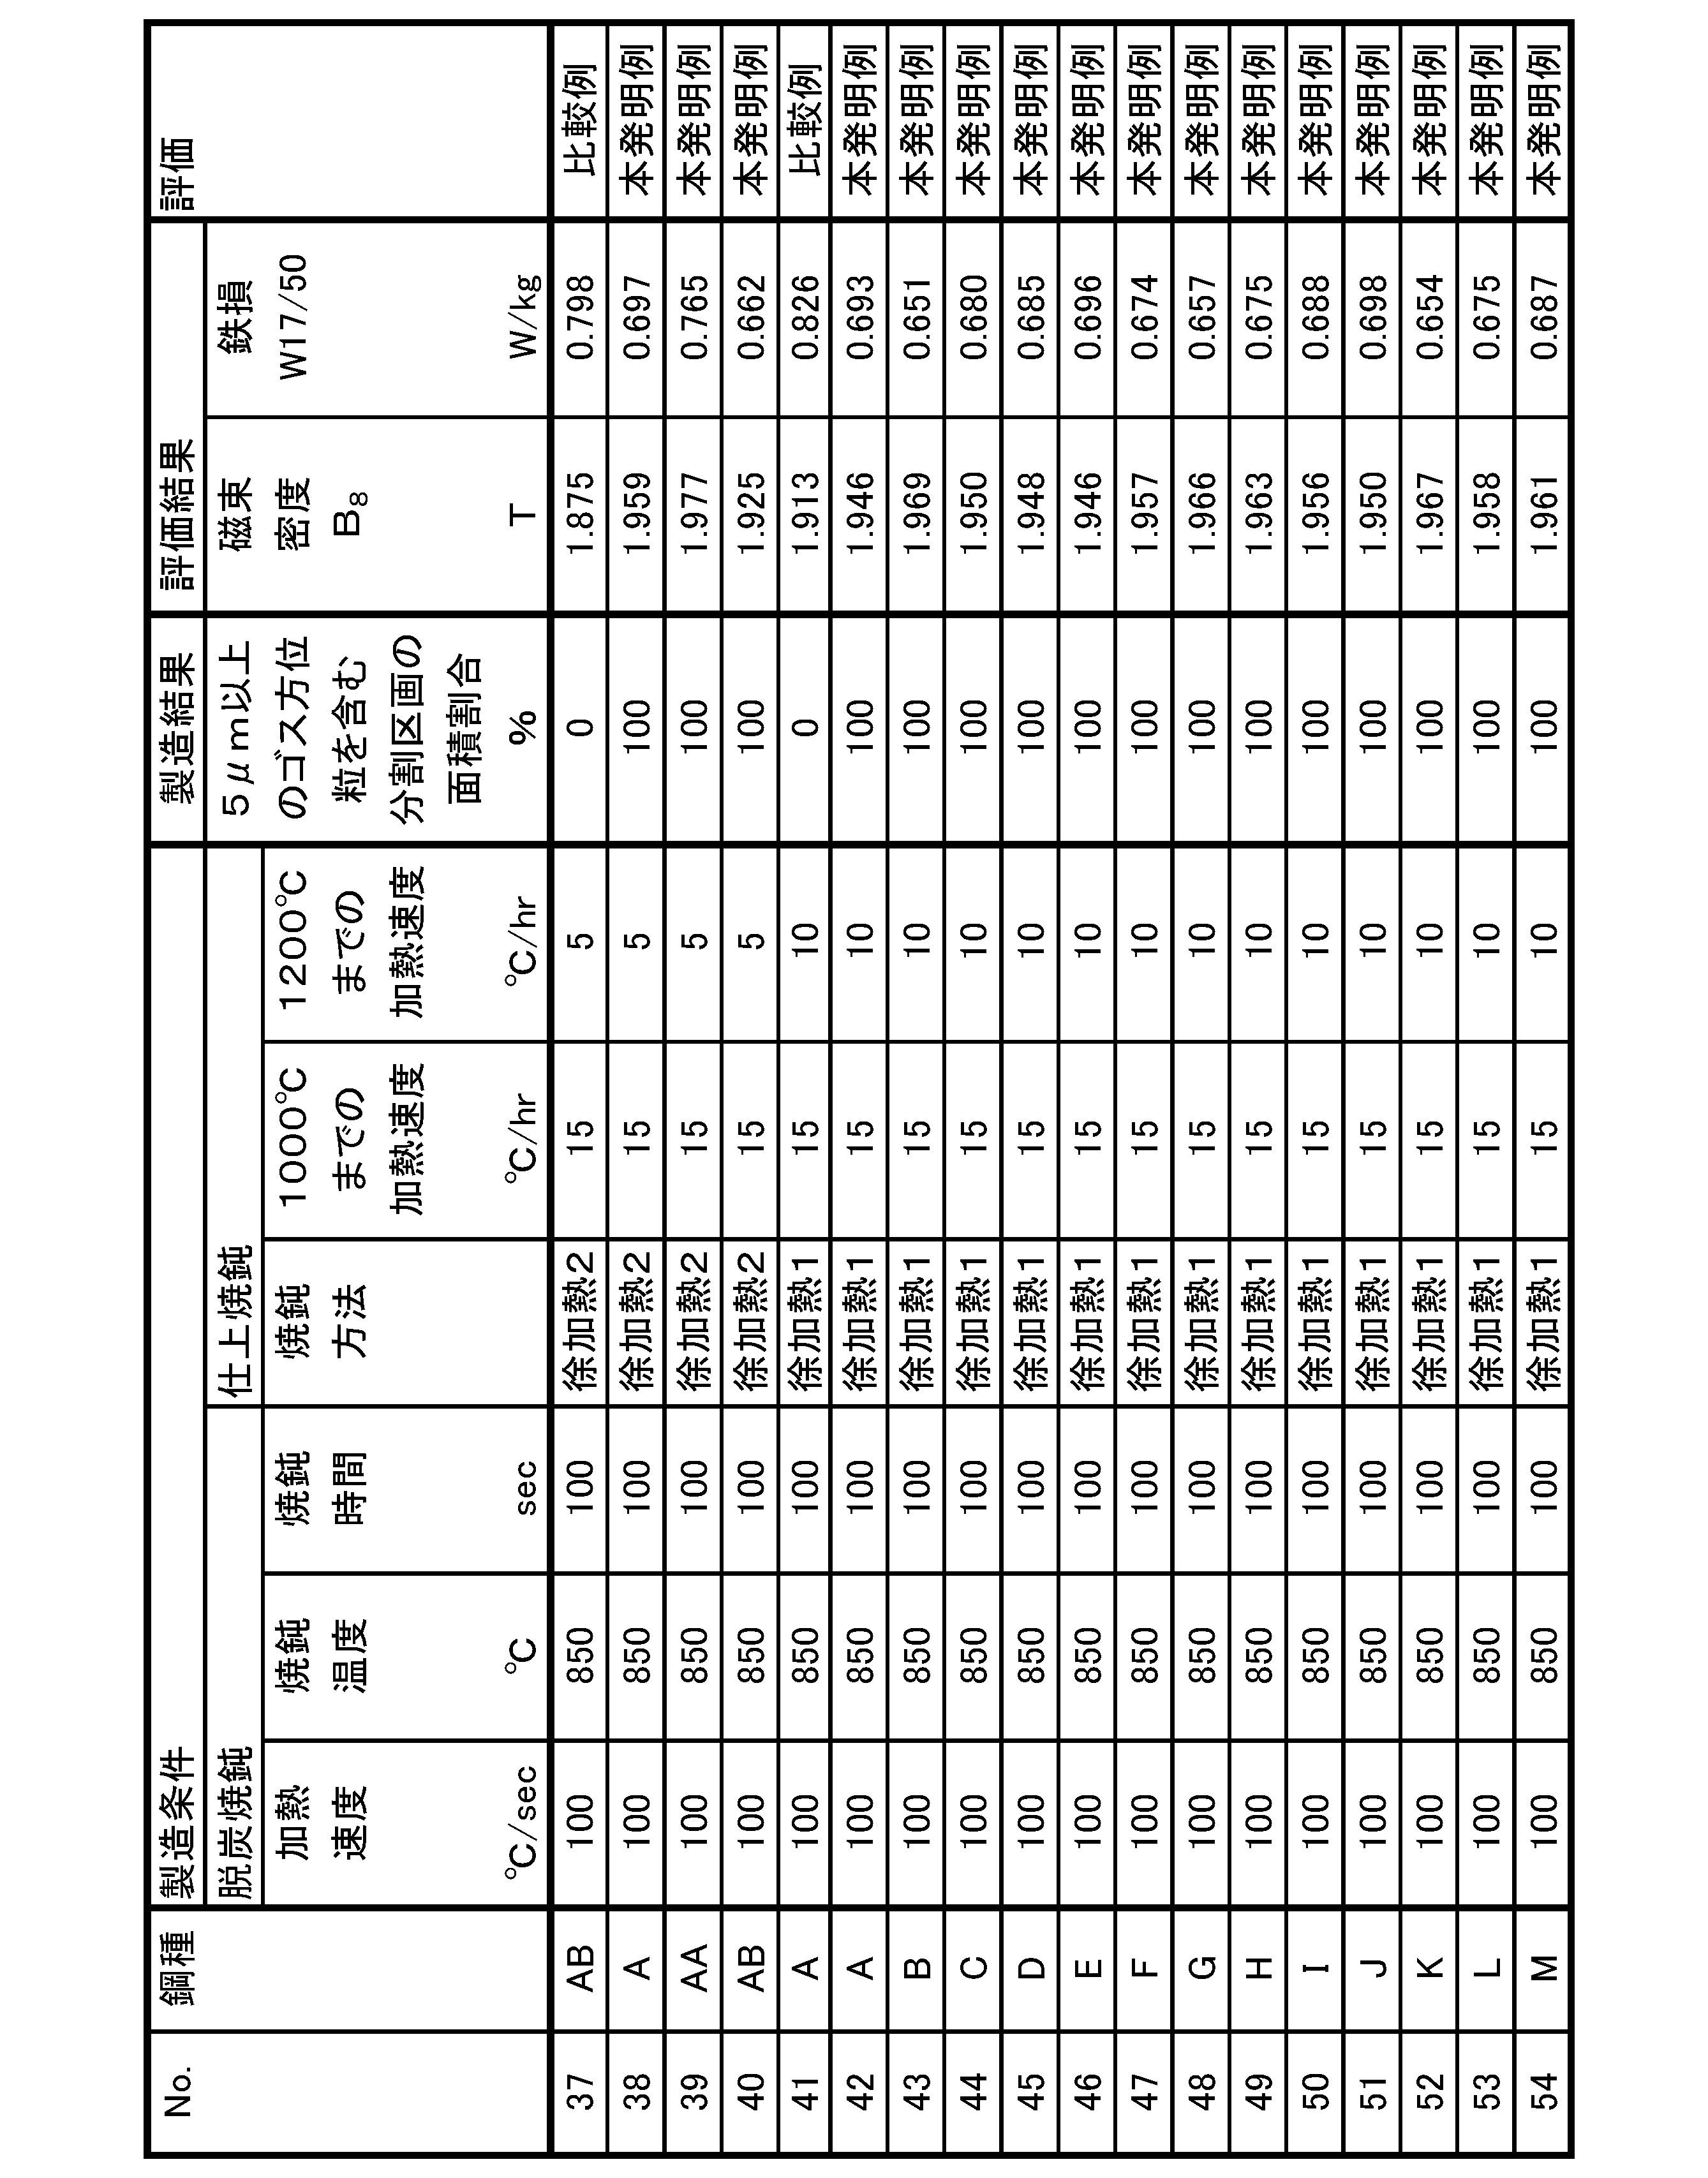
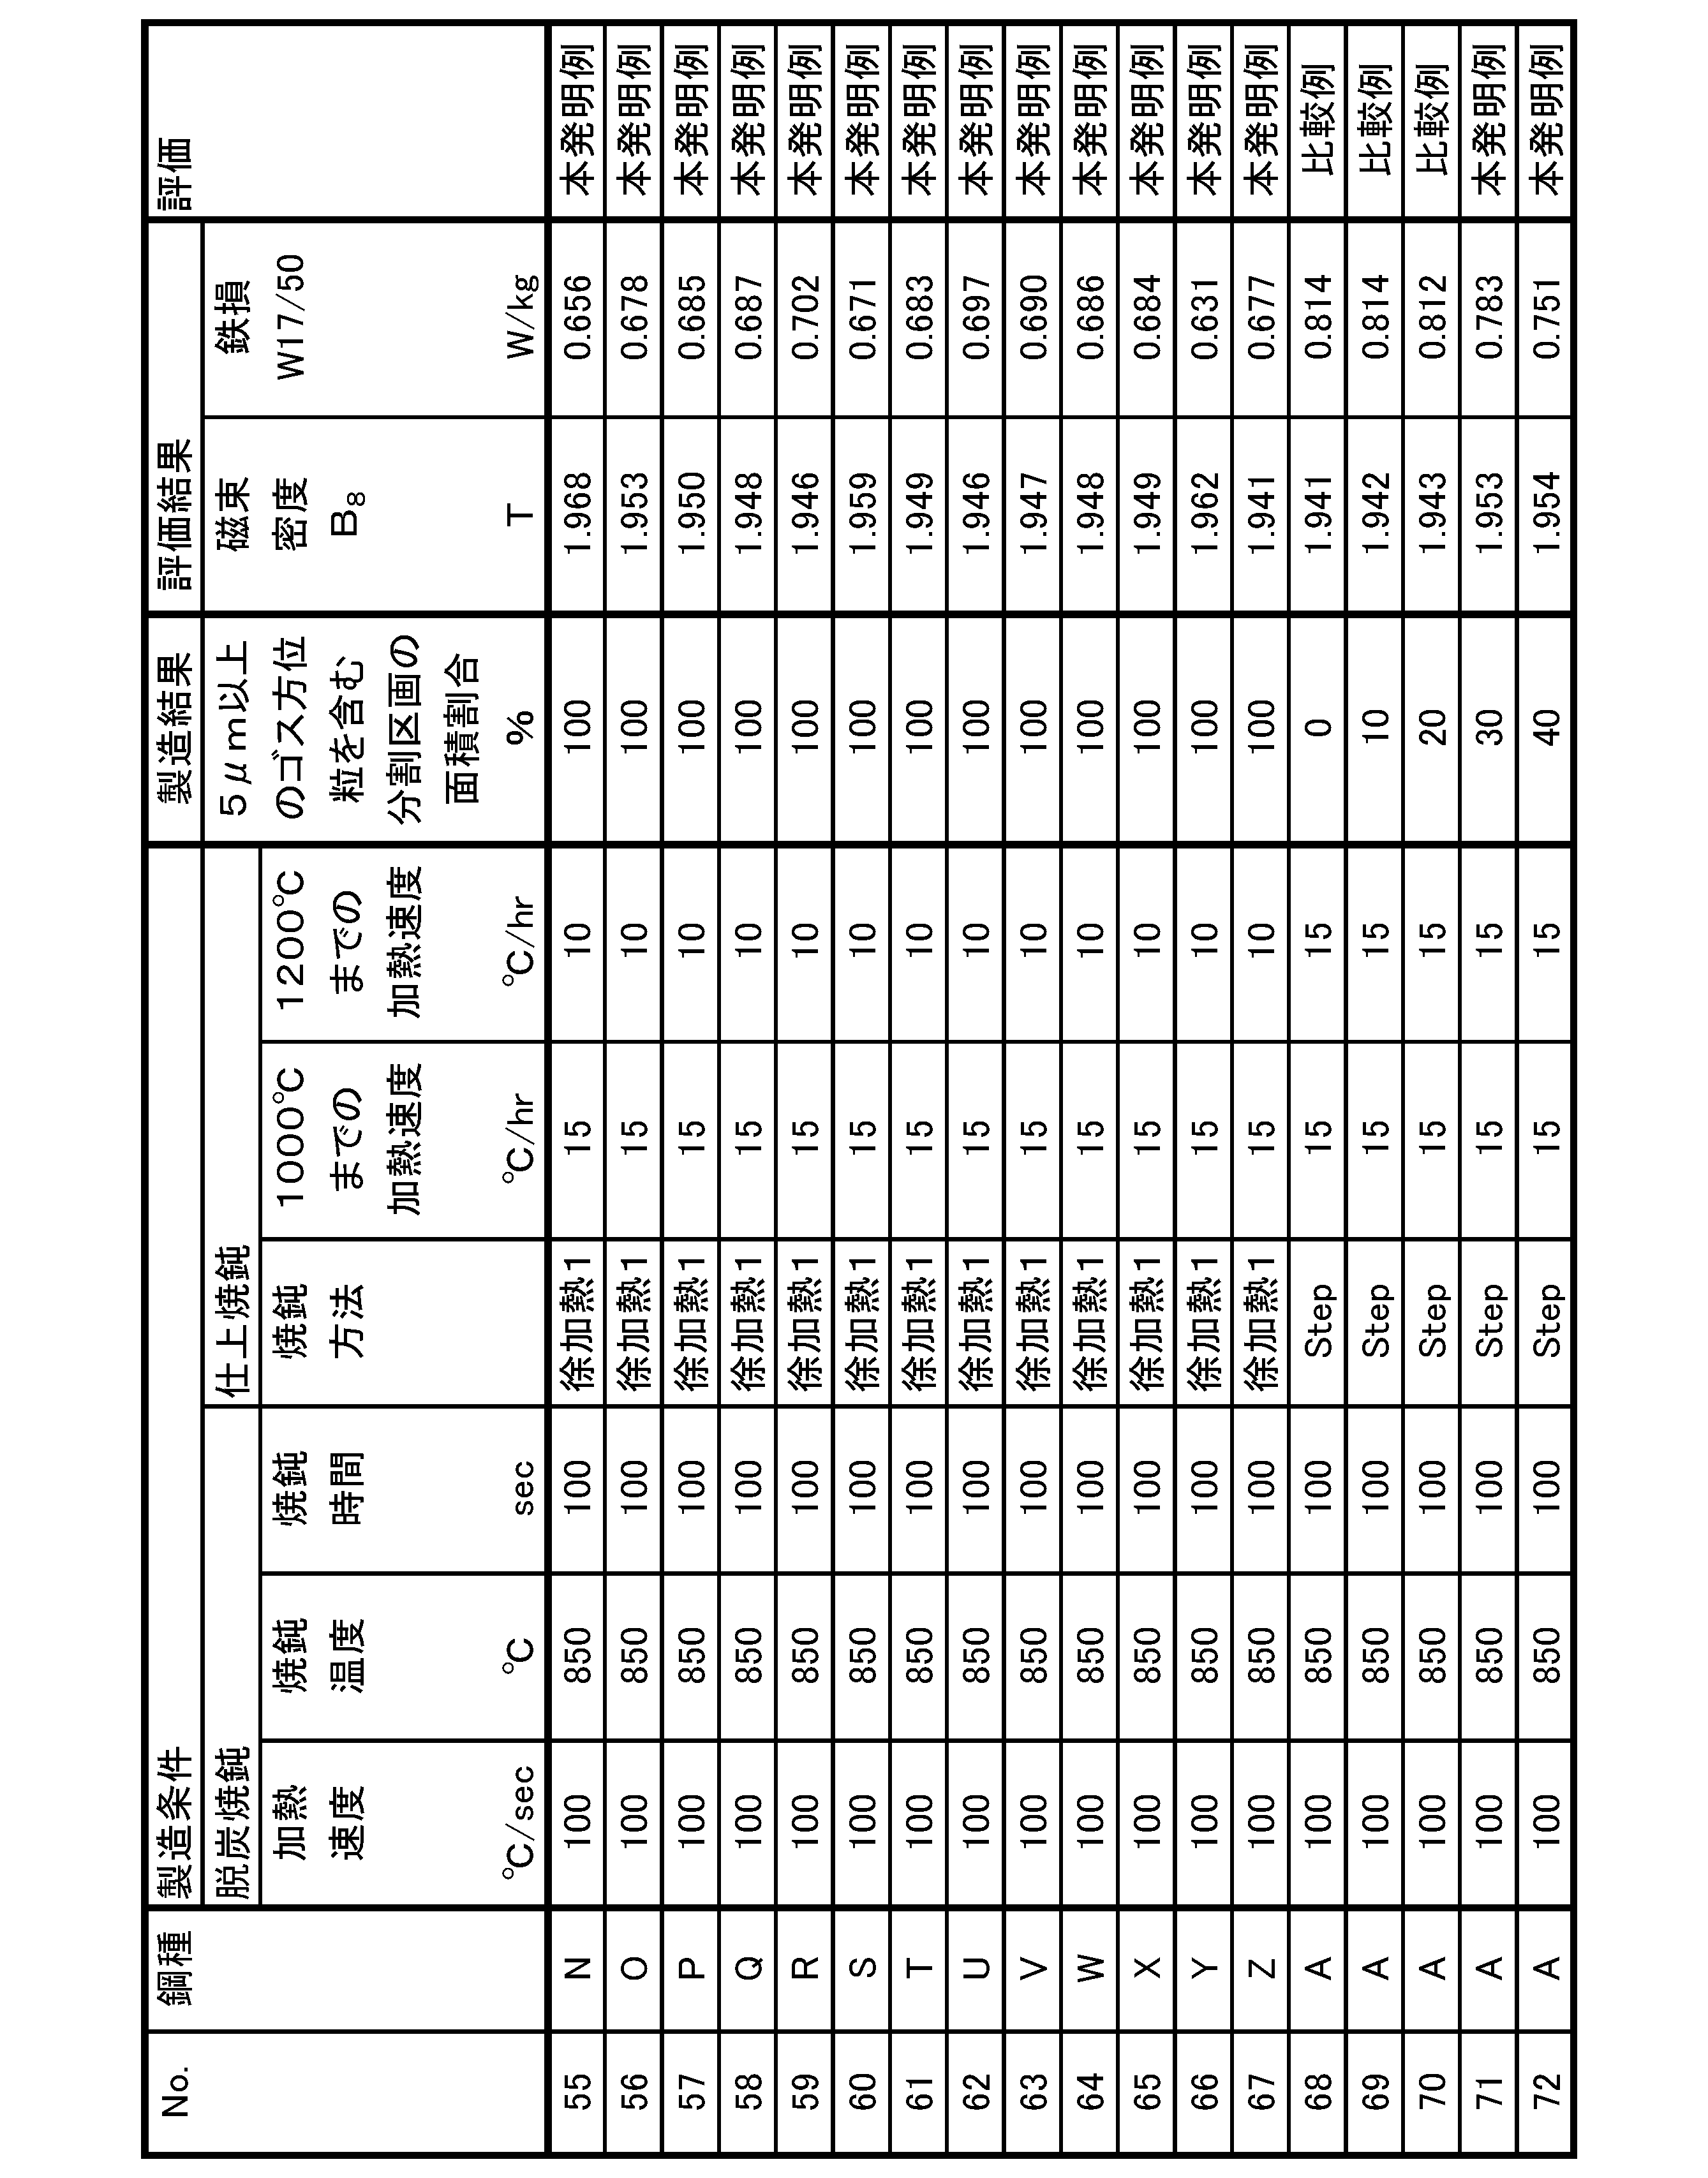

2 局所加熱領域
3 非局所加熱領域(マトリックス部)
4 局所加熱領域境界
14 ゴス方位粒
15 粗大ゴス方位粒(粒径が5μm以上のゴス方位粒)
21 圧延方向
22 幅方向(圧延直角方向)
Claims (1)
- 方向性電磁鋼板用の冷延鋼板であって、
圧延面法線方向を回転軸とする理想ゴス方位からのずれ角をαと定義し、
圧延直角方向を回転軸とする理想ゴス方位からのずれ角をβと定義し、
板面上の測定点で測定する結晶方位のずれ角を(α β)と表し、
前記測定点での角度偏差をφ=(α2+β2)1/2と定義し、
前記角度偏差φが10°以下である結晶粒をゴス方位粒と定義し、
板面上の100mm×100mmの領域を分割区画と定義し、
前記分割区画内に前記ゴス方位粒が含まれるかを、少なくとも100区画の分割区画で確認したとき、
5μm以上の粒径をもつゴス方位粒が少なくとも1つ含まれる分割区画が、すべての分割区画に対して、30面積%以上である
ことを特徴とする方向性電磁鋼板用の冷延鋼板。
Priority Applications (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP24832028.5A EP4737607A1 (en) | 2023-06-29 | 2024-06-27 | Cold-rolled steel sheet |
| KR1020267001114A KR20260021783A (ko) | 2023-06-29 | 2024-06-27 | 냉연 강판 |
| JP2025530187A JPWO2025005169A1 (ja) | 2023-06-29 | 2024-06-27 | |
| CN202480041712.XA CN121399282A (zh) | 2023-06-29 | 2024-06-27 | 冷轧钢板 |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP2023-106555 | 2023-06-29 | ||
| JP2023106555 | 2023-06-29 |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| WO2025005169A1 true WO2025005169A1 (ja) | 2025-01-02 |
Family
ID=93939149
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| PCT/JP2024/023290 Ceased WO2025005169A1 (ja) | 2023-06-29 | 2024-06-27 | 冷延鋼板 |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP4737607A1 (ja) |
| JP (1) | JPWO2025005169A1 (ja) |
| KR (1) | KR20260021783A (ja) |
| CN (1) | CN121399282A (ja) |
| WO (1) | WO2025005169A1 (ja) |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH10183312A (ja) * | 1996-10-21 | 1998-07-14 | Kawasaki Steel Corp | 鉄損が低く、耐歪特性および実機特性に優れた方向性電磁鋼板およびその製造方法 |
| JPH10183313A (ja) * | 1996-10-21 | 1998-07-14 | Kawasaki Steel Corp | 鉄損が低く、耐歪特性および実機特性に優れた方向性電磁鋼板 |
| JP2007169762A (ja) | 2005-12-26 | 2007-07-05 | Jfe Steel Kk | 低鉄損方向性電磁鋼板の製造方法 |
| JP2008261022A (ja) * | 2007-04-13 | 2008-10-30 | Nippon Steel Corp | 方向性電磁鋼板脱炭焼鈍板及びその製造方法 |
| WO2012014290A1 (ja) | 2010-07-28 | 2012-02-02 | 新日本製鐵株式会社 | 方向性電磁鋼板及びその製造方法 |
| JP2019506528A (ja) * | 2015-12-23 | 2019-03-07 | ポスコPosco | 方向性電磁鋼板およびその製造方法 |
| JP2022161269A (ja) | 2021-04-08 | 2022-10-21 | 日本製鉄株式会社 | 方向性電磁鋼板の製造方法 |
| JP2023106555A (ja) | 2019-07-03 | 2023-08-01 | 株式会社北電子 | 遊技機 |
-
2024
- 2024-06-27 JP JP2025530187A patent/JPWO2025005169A1/ja active Pending
- 2024-06-27 WO PCT/JP2024/023290 patent/WO2025005169A1/ja not_active Ceased
- 2024-06-27 KR KR1020267001114A patent/KR20260021783A/ko active Pending
- 2024-06-27 EP EP24832028.5A patent/EP4737607A1/en active Pending
- 2024-06-27 CN CN202480041712.XA patent/CN121399282A/zh active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JPH10183312A (ja) * | 1996-10-21 | 1998-07-14 | Kawasaki Steel Corp | 鉄損が低く、耐歪特性および実機特性に優れた方向性電磁鋼板およびその製造方法 |
| JPH10183313A (ja) * | 1996-10-21 | 1998-07-14 | Kawasaki Steel Corp | 鉄損が低く、耐歪特性および実機特性に優れた方向性電磁鋼板 |
| JP2007169762A (ja) | 2005-12-26 | 2007-07-05 | Jfe Steel Kk | 低鉄損方向性電磁鋼板の製造方法 |
| JP2008261022A (ja) * | 2007-04-13 | 2008-10-30 | Nippon Steel Corp | 方向性電磁鋼板脱炭焼鈍板及びその製造方法 |
| WO2012014290A1 (ja) | 2010-07-28 | 2012-02-02 | 新日本製鐵株式会社 | 方向性電磁鋼板及びその製造方法 |
| JP2019506528A (ja) * | 2015-12-23 | 2019-03-07 | ポスコPosco | 方向性電磁鋼板およびその製造方法 |
| JP2023106555A (ja) | 2019-07-03 | 2023-08-01 | 株式会社北電子 | 遊技機 |
| JP2022161269A (ja) | 2021-04-08 | 2022-10-21 | 日本製鉄株式会社 | 方向性電磁鋼板の製造方法 |
Also Published As
| Publication number | Publication date |
|---|---|
| CN121399282A (zh) | 2026-01-23 |
| JPWO2025005169A1 (ja) | 2025-01-02 |
| EP4737607A1 (en) | 2026-05-06 |
| KR20260021783A (ko) | 2026-02-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105579596B (zh) | 取向性电磁钢板的制造方法 | |
| CN104220607B (zh) | 取向性电磁钢板的制造方法 | |
| JP5691265B2 (ja) | 方向性電磁鋼板の製造方法 | |
| JPWO2016056501A1 (ja) | 低鉄損方向性電磁鋼板およびその製造方法 | |
| US20200032363A1 (en) | Method for producing grain-oriented electrical steel sheet | |
| JP6160649B2 (ja) | 方向性電磁鋼板の製造方法 | |
| CN111417737B (zh) | 低铁损取向性电磁钢板及其制造方法 | |
| JP7606155B1 (ja) | 方向性電磁鋼板 | |
| JP7644338B2 (ja) | 方向性電磁鋼板の製造方法 | |
| JP7606154B1 (ja) | 方向性電磁鋼板 | |
| WO2017111509A1 (ko) | 방향성 전기강판 및 그 제조방법 | |
| JP7818602B2 (ja) | 方向性電磁鋼板およびその製造方法 | |
| MX2012015155A (es) | Metodo para la produccion de chapa de acero magnetica de grano orientado. | |
| CN107406936A (zh) | 取向性电磁钢板及其制造方法 | |
| JP2012177162A (ja) | 方向性電磁鋼板の製造方法 | |
| JP2012067349A (ja) | 方向性電磁鋼板の製造方法 | |
| JP7787485B2 (ja) | 方向性電磁鋼板用の脱炭焼鈍鋼板 | |
| KR20260021783A (ko) | 냉연 강판 | |
| JP7538460B1 (ja) | 鉄損特性に優れた方向性電磁鋼板 | |
| US20250051867A1 (en) | Grain oriented electrical steel sheet and method for manufacturing same | |
| WO2025005170A1 (ja) | 方向性電磁鋼板 | |
| JP2024546161A (ja) | 方向性電磁鋼板およびその製造方法 | |
| WO2026014484A1 (ja) | 方向性電磁鋼板の製造方法 | |
| WO2025187777A1 (ja) | 脱炭焼鈍鋼板 | |
| JP2025151626A (ja) | 方向性電磁鋼板の製造方法 |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| 121 | Ep: the epo has been informed by wipo that ep was designated in this application |
Ref document number: 24832028 Country of ref document: EP Kind code of ref document: A1 |
|
| ENP | Entry into the national phase |
Ref document number: 2025530187 Country of ref document: JP Kind code of ref document: A |
|
| REG | Reference to national code |
Ref country code: BR Ref legal event code: B01A Ref document number: 112025028417 Country of ref document: BR |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 202517133405 Country of ref document: IN |
|
| ENP | Entry into the national phase |
Ref document number: 1020267001114 Country of ref document: KR Free format text: ST27 STATUS EVENT CODE: A-0-1-A10-A15-NAP-PA0105 (AS PROVIDED BY THE NATIONAL OFFICE) |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 1020267001114 Country of ref document: KR |
|
| WWP | Wipo information: published in national office |
Ref document number: 202517133405 Country of ref document: IN |
|
| WWE | Wipo information: entry into national phase |
Ref document number: 2024832028 Country of ref document: EP Ref document number: 2026100853 Country of ref document: RU |
|
| NENP | Non-entry into the national phase |
Ref country code: DE |
|
| ENP | Entry into the national phase |
Ref document number: 2024832028 Country of ref document: EP Effective date: 20260129 |
|
| ENP | Entry into the national phase |
Ref document number: 2024832028 Country of ref document: EP Effective date: 20260129 |
|
| WWP | Wipo information: published in national office |
Ref document number: 1020267001114 Country of ref document: KR |
|
| WWP | Wipo information: published in national office |
Ref document number: 2026100853 Country of ref document: RU |
|
| WWP | Wipo information: published in national office |
Ref document number: 2024832028 Country of ref document: EP |