EP4305975B1 - Filter rod having hollow outer section and filled inner core, and processing method therefor - Google Patents
Filter rod having hollow outer section and filled inner core, and processing method therefor Download PDFInfo
- Publication number
- EP4305975B1 EP4305975B1 EP23772391.1A EP23772391A EP4305975B1 EP 4305975 B1 EP4305975 B1 EP 4305975B1 EP 23772391 A EP23772391 A EP 23772391A EP 4305975 B1 EP4305975 B1 EP 4305975B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- forming
- mouth
- trumpet
- filter stick
- forming paper
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

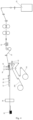
Classifications
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/04—Tobacco smoke filters characterised by their shape or structure
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/0229—Filter rod forming processes
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/025—Final operations, i.e. after the filter rod forming process
- A24D3/0254—Cutting means
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/0275—Manufacture of tobacco smoke filters for filters with special features
- A24D3/0287—Manufacture of tobacco smoke filters for filters with special features for composite filters
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/02—Manufacture of tobacco smoke filters
- A24D3/0275—Manufacture of tobacco smoke filters for filters with special features
- A24D3/0291—Manufacture of tobacco smoke filters for filters with special features for hollow tipped filters, e.g. recess filters
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/06—Use of materials for tobacco smoke filters
- A24D3/061—Use of materials for tobacco smoke filters containing additives entrapped within capsules, sponge-like material or the like, for further release upon smoking
-
- A—HUMAN NECESSITIES
- A24—TOBACCO; CIGARS; CIGARETTES; SIMULATED SMOKING DEVICES; SMOKERS' REQUISITES
- A24D—CIGARS; CIGARETTES; TOBACCO SMOKE FILTERS; MOUTHPIECES OF CIGARS OR CIGARETTES; MANUFACTURE OF TOBACCO SMOKE FILTERS OR MOUTHPIECES
- A24D3/00—Tobacco smoke filters, e.g. filter tips or filtering inserts; Filters specially adapted for simulated smoking devices; Mouthpieces of cigars or cigarettes
- A24D3/06—Use of materials for tobacco smoke filters
- A24D3/08—Use of materials for tobacco smoke filters of organic materials as carrier or major constituent
- A24D3/10—Use of materials for tobacco smoke filters of organic materials as carrier or major constituent of cellulose or cellulose derivatives
Definitions
- the present invention belongs to the technical field of tobacco and provides a forming method of an externally-hollow filter stick with a filled core.
- a tobacco material with a single function hardly meets demands of cigarette brand development and product characteristics.
- the tobacco material has been developed from the single function to multiple functions and diversified directions.
- a filter stick serves as an important composition part of a cigarette, and more and more hollow filter sticks are applied to the cigarette due to their special functions.
- Cigarette flavoring plays a role in improving a physicochemical property of the cigarette, so the consumers have specific taste, smell and touch feeling and acceptability of the cigarette is improved.
- flavoring methods such as directly adding into cut tobacco or adding into other accessories of the cigarette, such as a filter tip, cigarette paper and a packaging material.
- a microcapsule in a tobacco product is put at a joint between the filter tip and a cigarette, or may also be gathered in a middle section of the filter tip to form the filter tip, and plays a different role during smoking, and a flavoring substance maintains an original flavor and meanwhile can effectively highlight a flavor of the cigarette product, cover unfavorable smell and improve a smoking sensation.
- Hollow filter sticks disclosed by patents CN210076559U , CN210382609U and CN105342005A each have a plurality of layers, and each layer is filled with tows.
- the hollow filter sticks in the above patents each need a pressure-reduced channel or groove formed by folding forming paper, these pressure-reduced channels or grooves are complicated in shape and difficult for large-scale industrial production.
- the present invention as defined in claim 1, is provided for solving the above problems.
- the present invention discloses in claim 1 a forming method of an externally-hollow filter stick with a filled core.
- a first aspect is represented by an externally-hollow filter stick with a filled core.
- the externally-hollow filter stick with the filled core is cylindrical in appearance and is composed of an outer layer which is a cylinder W1 formed by rolling outer forming paper W and an inner layer which is in a cylindrical shape with a cross section being a regular triangle N1 in an axial direction of the cylinder W1 formed by folding inner forming paper N; and three vertexes of the regular triangle N1 are on an inner wall surface of the cylinder W1, wherein an interior of the inner forming paper N is filled with inner tows S2.
- the quantity of the inner forming paper N is 30-40 g/m 2 .
- the quantity of the outer forming paper W is 90-110 g/m 2 .
- the regular triangle N1 is formed by folding two layers of second forming paper 2.
- the inner tows S2 are 3.0-12.0 Y in denier per filament and 15000-35000 D in denier of all filaments; and generally, 3.9 Y/31000 D, 3.0 Y/32000 D, 3.0 Y/35000 D or 3.8 Y/34000 D, which may be selected according to a design requirement of the filter stick.
- a common filter stick is 3.0-3.9 Y and 31000-35000 D
- a medium filter stick is 3.8-6.7 Y and 22000-34000 D
- a fine filter stick is 6.0-12.0 Y and 15000-16000 D.
- the inner and outer layers of forming paper may be flavored separately or simultaneously.
- a second aspect is represented by a forming method of an externally-hollow filter stick with a filled core, which uses a filter stick one-time forming system.
- the filter stick one-time forming system includes the following components: a forming trumpet-like mouth C, an outer forming paper conveying belt 3W, an inner forming paper conveying belt 3N and an inner tow conveying belt 52; the forming trumpet-like mouth C includes an outer forming trumpet-like mouth 11 and an inner forming trumpet-like mouth 21, and the inner forming trumpet-like mouth 21 is sleeved with the outer forming trumpet-like mouth 11; the outer forming trumpet-like mouth 11 is in a cylindrical shape with a radius decreasing gradually; and the inner forming trumpet-like mouth 21 has two layers, an outer layer 211 is in a cylindrical shape which transits gradually from a circle to a regular triangle, and an inner layer 212 is in a triangular prism shape with one end being a large-area regular triangle and the other end being a small-area regular triangle.
- the forming method of the externally-hollow filter stick with the filled core includes the following steps: conveying outer forming paper W by the outer forming paper conveying belt 3W to an inlet of the forming trumpet-like mouth C to be baked by an outer forming paper baking device 31 and then enter a cylinder of the outer forming trumpet-like mouth 11 to be formed as a cylinder W1 shape and applied with an adhesive by an outer lap adhesive device 33 to come out of an outlet of the outer forming trumpet-like mouth 11; meanwhile, conveying inner forming paper N by the inner forming paper conveying belt 3N to the inlet of the forming trumpet-like mouth C to be baked by an inner forming paper baking device 32 and then enter a position between the outer layer 211 and the inner layer 212 of the inner forming trumpet-like mouth 21 to be formed gradually as a cylinder of the regular triangle N1 and applied with an adhesive by an inner lap adhesive device 33 to come out of an outlet of the inner forming trumpet-like mouth 21; at the moment, delivering inner tows S2 conveye
- the externally-hollow filter stick with the filled core obtained by the present invention may be used as a base stick A, the base stick A and another filter stick B of different types such as a filter capsule filter stick, a particle filter stick and a flavored filter stick are subjected to one-time combination according to a certain sequence and length ratio, so as to prepare an externally-hollow binary filter stick with a filled core, and the base stick A and the filter sticks B1 and B2 are subjected to two-time recombination according to a certain sequence and length ratio, so as to prepare an externally-hollow ternary filter stick with a filled core.
- the filter stick is put on a cigarette making machine to be connected with a cigarette, and then the externally-hollow filter stick with the filled core is arranged at a lip end of the cigarette.
- An experiment method without indicating specific conditions in the embodiment usually adopts a normal condition as well as a condition in a manual, or a general device, a material, a reagent and the like used in a condition recommended by a manufacturer, which may be commercially available without additional comments.
- Raw materials needed in the following embodiment and comparative example are available in the market.
- Fig. 1 is a schematic diagram of a cross section of a vertical center axis of an externally-hollow filter stick with a filled core in the present invention.
- a first aspect of the present invention discloses an externally-hollow filter stick with a filled core.
- the externally-hollow filter stick with the filled core is cylindrical in appearance and is composed of an outer layer which is a cylinder W1 formed by rolling outer forming paper W and an inner layer which is in a cylindrical shape with a cross section being a regular triangle N1 in an axial direction of the cylinder W1 formed by folding inner forming paper N; and three vertexes of the regular triangle N1 are on an inner wall surface of the cylinder W1, wherein an interior of the inner forming paper N is filled with inner tows S2.
- the quantity of the inner forming paper N is 30-40 g/m 2 .
- the quantity of the outer forming paper W is 90-110 g/m 2 .
- the regular triangle N1 is formed by folding two layers of second forming paper 2.
- the inner tows S2 are 3.0-12.0 Y in denier per filament and 15000-35000 D in denier of all filaments.
- a second aspect of the present invention discloses a forming method of an externally-hollow filter stick with a filled core, which uses a filter stick one-time forming system.
- the filter stick one-time forming system includes the following components: a forming trumpet-like mouth C, an outer forming paper conveying belt 3W, an inner forming paper conveying belt 3N and an inner tow conveying belt 52.
- the forming trumpet-like mouth C includes an outer forming trumpet-like mouth 11 and an inner forming trumpet-like mouth 21, and the inner forming trumpet-like mouth 11 is sleeved with the outer forming trumpet-like mouth 21; the outer forming trumpet-like mouth 11 is in a cylindrical shape with a radius decreasing gradually.
- the inner forming trumpet-like mouth 21 has two layers, an outer layer 211 is in a cylindrical shape which transits gradually from a circle to a regular triangle, and an inner layer 212 is in a triangular prism shape with one end being a large-area regular triangle and the other end being a small-area regular triangle.
- the forming method of the triangular filter stick with the filled core includes the following steps: outer forming paper W is conveyed by the outer forming paper conveying belt 3W to an inlet of the forming trumpet-like mouth C to be baked by an outer forming paper baking device 31 and then enter a cylinder of the outer forming trumpet-like mouth 11 to be formed as a cylinder W1 shape and applied with an adhesive by an outer lap adhesive device 33 to come out of an outlet of the outer forming trumpet-like mouth 11; meanwhile, inner forming paper N is conveyed by the inner forming paper conveying belt 3N to the inlet of the forming trumpet-like mouth C to be baked by an inner forming paper baking device 32 and then enter a position between the outer layer 211 and the inner layer 212 of the inner forming trumpet-like mouth 21 to be formed gradually as a cylinder of the regular triangle N1 and applied with an adhesive by an inner lap adhesive device 33 to come out of an outlet of the inner forming trumpet-like mouth 21; at the moment, inner tows S2 conveye
- the externally-hollow filter stick with the filled core prepared in the present invention is used as a base stick A, the base stick A and another filter stick B of different types such as a filter capsule filter stick, a particle filter stick and a flavored filter stick are subjected to one-time combination according to a certain sequence and length ratio, so as to prepare an externally-hollow binary filter stick with a filled core, and the base stick A and the filter sticks B1 and B2 are subjected to two-time recombination according to a certain sequence and length ratio, so as to prepare an externally-hollow ternary filter stick with a filled core.
- the filter stick is put on a cigarette making machine to be connected with a cigarette, and then the externally-hollow filter stick with the filled core is arranged at a lip end of the cigarette.
- the filter stick prepared through the method of the present invention is connected with a prepared cigarette, smoke gas is gathered and softer and more delicate, smoothness is good with clustering, smoking quality is mellow, convergence is high, the aroma quality and the aroma volume are improved, and sensory quality of cigarette may be improved effectively.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Cigarettes, Filters, And Manufacturing Of Filters (AREA)
Description
- The present invention belongs to the technical field of tobacco and provides a forming method of an externally-hollow filter stick with a filled core.
- With intensifying competition of the tobacco industry market, a tobacco material with a single function hardly meets demands of cigarette brand development and product characteristics. With application of a new technology, a new process and a new material in a tobacco product, the tobacco material has been developed from the single function to multiple functions and diversified directions. With increasingly intense competition of the cigarette market, a cigarette product with a novel appearance and special functions is of interest to consumers, a filter stick serves as an important composition part of a cigarette, and more and more hollow filter sticks are applied to the cigarette due to their special functions.
- Cigarette flavoring plays a role in improving a physicochemical property of the cigarette, so the consumers have specific taste, smell and touch feeling and acceptability of the cigarette is improved. There are many types of flavoring methods, such as directly adding into cut tobacco or adding into other accessories of the cigarette, such as a filter tip, cigarette paper and a packaging material. A microcapsule in a tobacco product is put at a joint between the filter tip and a cigarette, or may also be gathered in a middle section of the filter tip to form the filter tip, and plays a different role during smoking, and a flavoring substance maintains an original flavor and meanwhile can effectively highlight a flavor of the cigarette product, cover unfavorable smell and improve a smoking sensation.
- Hollow filter sticks disclosed by patents
CN210076559U ,CN210382609U andCN105342005A each have a plurality of layers, and each layer is filled with tows. The hollow filter sticks in the above patents each need a pressure-reduced channel or groove formed by folding forming paper, these pressure-reduced channels or grooves are complicated in shape and difficult for large-scale industrial production. - The prior art document
WO 2019/110715 A1 describes a conventional tobacco smoke filter and corresponding manufacturing method. - The present invention, as defined in claim 1, is provided for solving the above problems.
- The present invention discloses in claim 1 a forming method of an externally-hollow filter stick with a filled core.
- A technical solution in accordance with the present invention is as follows.
- A first aspect is represented by an externally-hollow filter stick with a filled core. The externally-hollow filter stick with the filled core is cylindrical in appearance and is composed of an outer layer which is a cylinder W1 formed by rolling outer forming paper W and an inner layer which is in a cylindrical shape with a cross section being a regular triangle N1 in an axial direction of the cylinder W1 formed by folding inner forming paper N; and three vertexes of the regular triangle N1 are on an inner wall surface of the cylinder W1, wherein an interior of the inner forming paper N is filled with inner tows S2.
- The quantity of the inner forming paper N is 30-40 g/m2.
- The quantity of the outer forming paper W is 90-110 g/m2.
- The regular triangle N1 is formed by folding two layers of second forming
paper 2. - The inner tows S2 are 3.0-12.0 Y in denier per filament and 15000-35000 D in denier of all filaments; and generally, 3.9 Y/31000 D, 3.0 Y/32000 D, 3.0 Y/35000 D or 3.8 Y/34000 D, which may be selected according to a design requirement of the filter stick. Generally, a common filter stick is 3.0-3.9 Y and 31000-35000 D, a medium filter stick is 3.8-6.7 Y and 22000-34000 D, and a fine filter stick is 6.0-12.0 Y and 15000-16000 D.
- Preferably, the inner and outer layers of forming paper may be flavored separately or simultaneously.
- A second aspect is represented by a forming method of an externally-hollow filter stick with a filled core, which uses a filter stick one-time forming system.
- The filter stick one-time forming system includes the following components: a forming trumpet-like mouth C, an outer forming
paper conveying belt 3W, an inner formingpaper conveying belt 3N and an innertow conveying belt 52; the forming trumpet-like mouth C includes an outer forming trumpet-like mouth 11 and an inner forming trumpet-like mouth 21, and the inner forming trumpet-like mouth 21 is sleeved with the outer forming trumpet-like mouth 11; the outer forming trumpet-like mouth 11 is in a cylindrical shape with a radius decreasing gradually; and the inner forming trumpet-like mouth 21 has two layers, anouter layer 211 is in a cylindrical shape which transits gradually from a circle to a regular triangle, and aninner layer 212 is in a triangular prism shape with one end being a large-area regular triangle and the other end being a small-area regular triangle. - The forming method of the externally-hollow filter stick with the filled core includes the following steps: conveying outer forming paper W by the outer forming
paper conveying belt 3W to an inlet of the forming trumpet-like mouth C to be baked by an outer formingpaper baking device 31 and then enter a cylinder of the outer forming trumpet-like mouth 11 to be formed as a cylinder W1 shape and applied with an adhesive by an outer lapadhesive device 33 to come out of an outlet of the outer forming trumpet-like mouth 11; meanwhile, conveying inner forming paper N by the inner formingpaper conveying belt 3N to the inlet of the forming trumpet-like mouth C to be baked by an inner formingpaper baking device 32 and then enter a position between theouter layer 211 and theinner layer 212 of the inner forming trumpet-like mouth 21 to be formed gradually as a cylinder of the regular triangle N1 and applied with an adhesive by an inner lapadhesive device 33 to come out of an outlet of the inner forming trumpet-like mouth 21; at the moment, delivering inner tows S2 conveyed from an innertow conveying belt 52 into the inner forming paper N; sleeving the cylinder of the regular triangle N1 and the cylinder W1 coming out of the outlet of the outer forming trumpet-like mouth 11 together, and filling an interior of the inner forming paper N with the inner tows S2; and applying an adhesive to the formed filter stick by anadhesive device 35, then gluing three vertexes of the regular triangle N1 to an inner wall surface of the cylinder W1, heating by aheater 36, performing cooling forming by acooler 37, cutting by acutter 38 and then outputting by aseparator roll 39, so as to obtain the externally-hollow filter stick with the filled core. - The externally-hollow filter stick with the filled core obtained by the present invention may be used as a base stick A, the base stick A and another filter stick B of different types such as a filter capsule filter stick, a particle filter stick and a flavored filter stick are subjected to one-time combination according to a certain sequence and length ratio, so as to prepare an externally-hollow binary filter stick with a filled core, and the base stick A and the filter sticks B1 and B2 are subjected to two-time recombination according to a certain sequence and length ratio, so as to prepare an externally-hollow ternary filter stick with a filled core. The filter stick is put on a cigarette making machine to be connected with a cigarette, and then the externally-hollow filter stick with the filled core is arranged at a lip end of the cigarette.
- Beneficial effects of the present invention are:
- 1. By using the inner forming paper and the outer forming paper with different quantities in the present invention, the externally-hollow filter stick with the filled core is prepared, so that different functions are achieved; filtering permeability is improved through the outer layer, so easiness is improved; and a space of the inner layer is filled with tows, so that filtering efficiency may be improved. A hollow filter stick obtained through a method in the prior art cannot be internally filled with the tows due to thermoforming, differentiated processing by using an existing flavoring technology is unavailable, and a filtering effect of a hollow filter stick section is not achieved.
- 2. The present invention designs and prepares the forming trumpet-like mouth autonomously. The forming trumpet-like mouth includes the outer forming trumpet-like mouth and the inner forming trumpet-like mouth, and the inner forming trumpet-like mouth is sleeved with the outer forming trumpet-like mouth; the outer forming trumpet-like mouth is in a cylindrical shape with a radius decreasing gradually; and the inner forming trumpet-like mouth has two layers, an outer layer is in a cylindrical shape which transits gradually from a circle to a regular triangle, and an inner layer is in a triangular prism shape with one end being a large-area regular triangle and the other end being a small-area regular triangle. The forming trumpet-like mouth of the present invention easily make the inner forming paper and the outer forming paper form a required shape by one-time forming; and large-scale industrial production is easy.
- 3. The inner and outer layers of forming paper of the present invention are glued together, the inner layer of forming paper is filled with the tows, and there is a cavity between the outer layer of forming paper and the inner layer of forming paper, which is different from a position and a mechanism of a hollow structure in an existing hollow filter stick for smoke gas circulation; and the triangular filter stick with the filled core of the present invention may better gather smoke gas, smoke gas is softer and more delicate, smoothness is good with clustering, smoking quality is mellow, and convergence is high.
- 4. According to the externally-hollow filter stick with the filled core of the present invention, the inner layer is filled with the tows, forming paper flavoring and tow flavoring cooperate, so a flavoring effect of the tows may be better achieved, cigarette flavor is better gathered, cigarette aroma quality is improved, an aroma volume is enhanced, and sensory quality of the cigarette may be improved effectively.
-
-
Fig. 1 is a schematic diagram of a cross section of a vertical center axis of an externally-hollow filter stick with a filled core in accordance with the present invention. -
Fig. 2 is a schematic diagram of a forming trumpet-like mouth in accordance with the present invention. -
Fig. 3 is a schematic diagram of an inner forming trumpet-like mouth in accordance with the present invention. -
Fig. 4 is a schematic diagram of a one-time forming system of an externally-hollow filter stick with a filled core in accordance with the present invention. - Reference numerals: 11, outer forming trumpet-like mouth; 111, fixing point; 21, inner forming trumpet-like mouth; 211, outer layer; 212, inner layer; 3W, outer forming paper conveying belt; 3N, inner forming paper conveying belt; 31, outer forming paper baking device; 32, inner forming paper baking device; 33, inner lap adhesive device; 34, outer lap adhesive device; 35, adhesive device; 36, heater; 37, cooler; 38, cutter; 39, separator roll; 51, inner tow pack; 52, inner tow conveying belt; 53, inner additive box; W, outer forming paper; N, inner forming paper; W1, cylinder; N1, regular triangle, C, forming trumpet-like mouth; and S2, inner tow.
- The present invention is further described below through an embodiment but not limited to this embodiment. An experiment method without indicating specific conditions in the embodiment usually adopts a normal condition as well as a condition in a manual, or a general device, a material, a reagent and the like used in a condition recommended by a manufacturer, which may be commercially available without additional comments. Raw materials needed in the following embodiment and comparative example are available in the market.
- As shown in
Fig. 1, Fig. 1 is a schematic diagram of a cross section of a vertical center axis of an externally-hollow filter stick with a filled core in the present invention. A first aspect of the present invention discloses an externally-hollow filter stick with a filled core. The externally-hollow filter stick with the filled core is cylindrical in appearance and is composed of an outer layer which is a cylinder W1 formed by rolling outer forming paper W and an inner layer which is in a cylindrical shape with a cross section being a regular triangle N1 in an axial direction of the cylinder W1 formed by folding inner forming paper N; and three vertexes of the regular triangle N1 are on an inner wall surface of the cylinder W1, wherein an interior of the inner forming paper N is filled with inner tows S2. The quantity of the inner forming paper N is 30-40 g/m2. The quantity of the outer forming paper W is 90-110 g/m2. The regular triangle N1 is formed by folding two layers of second formingpaper 2. The inner tows S2 are 3.0-12.0 Y in denier per filament and 15000-35000 D in denier of all filaments. - A second aspect of the present invention discloses a forming method of an externally-hollow filter stick with a filled core, which uses a filter stick one-time forming system.
- As shown in
Fig. 4 , the filter stick one-time forming system includes the following components: a forming trumpet-like mouth C, an outer formingpaper conveying belt 3W, an inner formingpaper conveying belt 3N and an innertow conveying belt 52. As shown inFig. 2 , the forming trumpet-like mouth C includes an outer forming trumpet-like mouth 11 and an inner forming trumpet-like mouth 21, and the inner forming trumpet-like mouth 11 is sleeved with the outer forming trumpet-like mouth 21; the outer forming trumpet-like mouth 11 is in a cylindrical shape with a radius decreasing gradually. As shown inFig. 3 , the inner forming trumpet-like mouth 21 has two layers, anouter layer 211 is in a cylindrical shape which transits gradually from a circle to a regular triangle, and aninner layer 212 is in a triangular prism shape with one end being a large-area regular triangle and the other end being a small-area regular triangle. - The forming method of the triangular filter stick with the filled core includes the following steps: outer forming paper W is conveyed by the outer forming
paper conveying belt 3W to an inlet of the forming trumpet-like mouth C to be baked by an outer formingpaper baking device 31 and then enter a cylinder of the outer forming trumpet-like mouth 11 to be formed as a cylinder W1 shape and applied with an adhesive by an outer lapadhesive device 33 to come out of an outlet of the outer forming trumpet-like mouth 11; meanwhile, inner forming paper N is conveyed by the inner formingpaper conveying belt 3N to the inlet of the forming trumpet-like mouth C to be baked by an inner formingpaper baking device 32 and then enter a position between theouter layer 211 and theinner layer 212 of the inner forming trumpet-like mouth 21 to be formed gradually as a cylinder of the regular triangle N1 and applied with an adhesive by an inner lapadhesive device 33 to come out of an outlet of the inner forming trumpet-like mouth 21; at the moment, inner tows S2 conveyed from an innertow conveying belt 52 are delivered into the inner forming paper N; the cylinder of the regular triangle N1 and the cylinder W1 coming out of the outlet of the outer forming trumpet-like mouth 11 are sleeved together, and an interior of the inner forming paper N is filled with the inner tows S2; and an adhesive is applied to the formed filter stick by anadhesive device 35, then three vertexes of the regular triangle N1 are glued to an inner wall surface of the cylinder W1, heating is performed by aheater 36, cooling forming is performed by acooler 37, cutting is performed by acutter 38 and then outputting is performed by aseparator roll 39, so as to obtain the externally-hollow filter stick with the filled core. - The externally-hollow filter stick with the filled core prepared in the present invention is used as a base stick A, the base stick A and another filter stick B of different types such as a filter capsule filter stick, a particle filter stick and a flavored filter stick are subjected to one-time combination according to a certain sequence and length ratio, so as to prepare an externally-hollow binary filter stick with a filled core, and the base stick A and the filter sticks B1 and B2 are subjected to two-time recombination according to a certain sequence and length ratio, so as to prepare an externally-hollow ternary filter stick with a filled core. The filter stick is put on a cigarette making machine to be connected with a cigarette, and then the externally-hollow filter stick with the filled core is arranged at a lip end of the cigarette.
- Running conditions of the method of the present invention and a method in the prior art and comparison of results of obtained cigarettes:
Production method Aroma quality Aroma volume Softness and delicacy Mellowne ss Convergence Sensory quality of cigarette Method of the present invention 14 16.5 5 5 4.5 91.5 Method in the prior art 13 14.5 3.5 3.5 3 90.0 - It may be known from the above comparison results that the filter stick prepared through the method of the present invention is connected with a prepared cigarette, smoke gas is gathered and softer and more delicate, smoothness is good with clustering, smoking quality is mellow, convergence is high, the aroma quality and the aroma volume are improved, and sensory quality of cigarette may be improved effectively.
- The above displays and describes a basic principle, main features and strengths of the present invention. Those skilled in the art should understand that the present invention is not limited to the above embodiment, descriptions in the above embodiment and the specification are only for explaining the principle of the present invention.
Claims (1)
- A forming method of an externally-hollow filter stick with a filled core,whereinthe externally-hollow filter stick is cylindrical in appearance and is composed of an outer layer which is a cylinder (W1) formed by rolling outer forming paper (W) and an inner layer which is in a cylindrical shape with a cross section being a regular triangle (N1) in an axial direction of the cylinder (W1) formed by folding inner forming paper (N); and wherein three vertexes of the regular triangle (N1) are on an inner wall surface of the cylinder (W1), wherein an interior of the inner forming paper (N) is filled with inner tows (S2);the quantity of the inner forming paper (N) is 30-40 g/m2;the quantity of the outer forming paper (W) is 90-110 g/m2;the regular triangle (N1) is formed by folding two layers of second forming paper (2);the inner tows (S2) are 3.0-12.0 denier per filament (Y) and 15000-35000 denier of all filaments (D);wherein the method uses a filter stick one-time forming system which comprises the following components:
a forming trumpet-like mouth (C), an outer forming paper conveying belt (3W), an inner forming paper conveying belt (3N) and an inner tow conveying belt (52); the forming trumpet-like mouth (C) comprises an outer forming trumpet-like mouth (11) and an inner forming trumpet-like mouth (21), and the inner forming trumpet-like mouth (21) is sleeved with the outer forming trumpet-like mouth (11); the outer forming trumpet-like mouth (11) is in a cylindrical shape with a radius decreasing gradually; and the inner forming trumpet-like mouth (21) has two layers, an outer layer (211) is in a cylindrical shape which transits gradually from a circle to a regular triangle, and an inner layer (212) is in a triangular prism shape with one end being a large-area regular triangle and the other end being a small-area regular triangle; andthe forming method of the externally-hollow filter stick with the filled core comprises the following steps: conveying the outer forming paper (W) by the outer forming paper conveying belt (3W) to an inlet of the forming trumpet-like mouth (C) to be baked by an outer forming paper baking device (31) and then entering a cylinder of the outer forming trumpet-like mouth (11) to be formed as the cylinder (W1) shape and being applied with an adhesive by an outer lap adhesive device (34) to come out of an outlet of the outer forming trumpet-like mouth (11); meanwhile, conveying the inner forming paper (N) by the inner forming paper conveying belt (3N) to the inlet of the forming trumpet-like mouth (C) to be baked by an inner forming paper baking device (32) and then entering a position between the outer layer (211) and the inner layer (212) of the inner forming trumpet-like mouth (21) to be formed gradually as a cylinder of the regular triangle (N1) and being applied with an adhesive by an inner lap adhesive device (33) to come out of an outlet of the inner forming trumpet-like mouth (21); at that moment, delivering the inner tows (S2) conveyed from an inner tow conveying belt (52) into the inner forming paper (N); sleeving the cylinder of the regular triangle (N1) and the cylinder (W1) coming out of the outlet of the outer forming trumpet-like mouth (11) together, and filling an interior of the inner forming paper (N) with the inner tows (S2); and applying an adhesive to the formed filter stick by an adhesive device (35), then gluing three vertexes of the regular triangle (N1) to an inner wall surface of the cylinder (W1), Performing heating by a heater (36), performing cooling forming by a cooler (37), performing cutting by a cutter (38) and then outputting the filter stick by a separator roll (39), so as to obtain the externally-hollow filter stick with the filled core.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202210568132.9A CN114983017B (en) | 2022-05-24 | 2022-05-24 | An outer hollow filter rod filled with an inner core and a processing method thereof |
| PCT/CN2023/080716 WO2023226522A1 (en) | 2022-05-24 | 2023-03-10 | Filter rod having hollow outer section and filled inner core, and processing method therefor |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP4305975A1 EP4305975A1 (en) | 2024-01-17 |
| EP4305975A4 EP4305975A4 (en) | 2024-05-15 |
| EP4305975B1 true EP4305975B1 (en) | 2024-08-21 |
Family
ID=83027824
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP23772391.1A Active EP4305975B1 (en) | 2022-05-24 | 2023-03-10 | Filter rod having hollow outer section and filled inner core, and processing method therefor |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4305975B1 (en) |
| CN (1) | CN114983017B (en) |
| WO (1) | WO2023226522A1 (en) |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114983015B (en) * | 2022-05-24 | 2026-06-02 | 云南中烟工业有限责任公司 | A sandwich-filled hollow triangular filter rod and its processing method |
| CN114983018B (en) * | 2022-05-24 | 2026-06-02 | 云南中烟工业有限责任公司 | A triangularly spaced hollow filter rod and its molding method |
| CN114983017B (en) * | 2022-05-24 | 2023-08-22 | 云南中烟工业有限责任公司 | An outer hollow filter rod filled with an inner core and a processing method thereof |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021083891A1 (en) * | 2019-10-28 | 2021-05-06 | Jt International Sa | Filter component for an aerosol-generating article |
Family Cites Families (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CA1212008A (en) * | 1981-12-23 | 1986-09-30 | Richard M. Berger | Smoke filter having extended film overwrap and method and apparatus for fabricating same |
| JP2955557B1 (en) * | 1998-05-08 | 1999-10-04 | 日本たばこ産業株式会社 | Sheath core type tobacco filter |
| JP3002173B2 (en) * | 1998-05-08 | 2000-01-24 | 日本たばこ産業株式会社 | Manufacturing method and device for tobacco filter |
| JP2955556B1 (en) * | 1998-05-08 | 1999-10-04 | 日本たばこ産業株式会社 | Tobacco filter |
| JP5877570B2 (en) * | 2012-11-26 | 2016-03-08 | 日本たばこ産業株式会社 | Filter cigarette manufacturing method, filter and filter cigarette |
| CN203207180U (en) * | 2013-02-05 | 2013-09-25 | 大亚科技股份有限公司 | Carbon-added polypropylene cigarette tow and cellulose acetate tow composite filtering nozzle bar |
| CN103222682A (en) * | 2013-04-09 | 2013-07-31 | 红云红河烟草(集团)有限责任公司 | Binary composite filter rod for cigarettes and its processing method and equipment |
| GB201420733D0 (en) * | 2014-11-21 | 2015-01-07 | British American Tobacco Co | Apparatus and method for filter manufacture |
| GB201501527D0 (en) * | 2015-01-30 | 2015-03-18 | British American Tobacco Co | Apparatus and method for filter manufacture |
| CN105342005A (en) | 2015-11-17 | 2016-02-24 | 南通烟滤嘴有限责任公司 | Coaxial filter rod with double permeability |
| CN205432111U (en) * | 2015-12-29 | 2016-08-10 | 蚌埠卷烟材料厂 | Coaxial core filter rod of abnormal shape |
| GB201720490D0 (en) * | 2017-12-08 | 2018-01-24 | Essentra Filter Products Dev Co Pte Ltd | Tobacco smoke filter |
| CN110353303A (en) * | 2018-04-09 | 2019-10-22 | 上海烟草集团有限责任公司 | A kind of special-shaped coaxial core filter stick and preparation method thereof |
| CN109043657A (en) * | 2018-06-29 | 2018-12-21 | 云南巴菰生物科技有限公司 | It is a kind of for heating the temperature adjustment filter stick for the tobacco product that do not burn |
| CN210382609U (en) | 2019-05-07 | 2020-04-24 | 牡丹江卷烟材料厂有限责任公司 | A coaxial hollow filter rod wrapped with grooved paper |
| CN210076559U (en) | 2019-05-07 | 2020-02-18 | 牡丹江卷烟材料厂有限责任公司 | Coaxial type special-shaped hollow filter rod |
| CN113424986B (en) * | 2021-07-26 | 2023-07-04 | 云南养瑞科技集团有限公司 | Fragrant cooling filter tip rod and preparation method thereof |
| CN114983017B (en) * | 2022-05-24 | 2023-08-22 | 云南中烟工业有限责任公司 | An outer hollow filter rod filled with an inner core and a processing method thereof |
-
2022
- 2022-05-24 CN CN202210568132.9A patent/CN114983017B/en active Active
-
2023
- 2023-03-10 WO PCT/CN2023/080716 patent/WO2023226522A1/en not_active Ceased
- 2023-03-10 EP EP23772391.1A patent/EP4305975B1/en active Active
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2021083891A1 (en) * | 2019-10-28 | 2021-05-06 | Jt International Sa | Filter component for an aerosol-generating article |
Also Published As
| Publication number | Publication date |
|---|---|
| EP4305975A1 (en) | 2024-01-17 |
| CN114983017B (en) | 2023-08-22 |
| EP4305975A4 (en) | 2024-05-15 |
| CN114983017A (en) | 2022-09-02 |
| WO2023226522A1 (en) | 2023-11-30 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP4305975A1 (en) | Filter rod having hollow outer section and filled inner core, and processing method therefor | |
| US12564214B2 (en) | Tobacco smoke filter and method of production | |
| US4357950A (en) | Tobacco smoke filter having improved tar/carbon monoxide ratio | |
| US4508525A (en) | Method and apparatus for producing tobacco smoke filter having improved tar/carbon monoxide ratio | |
| JP6370780B2 (en) | Cigarette smoke filter | |
| CN203662002U (en) | Tobacco smoke filter, tobacco smoke filter element and filter cigarette | |
| CN217446647U (en) | Filter rod one shot forming system | |
| CN114983016B (en) | Filter stick with triangular interval filling tows and processing method thereof | |
| EP3585188B1 (en) | Filter element and method for manufacturing thereof | |
| JP7733687B2 (en) | Manufacturing method of smoking article | |
| CN217592011U (en) | Forming horn mouth | |
| JP6462212B2 (en) | Cigarette smoking filter | |
| KR102937003B1 (en) | Method for forming a hollow triangular filter rod filled in layers | |
| KR102937002B1 (en) | Method for forming a completely hollow filter rod with triangular spacing | |
| CN217509870U (en) | Filter rod with triangular interval filling tows | |
| CN115486558A (en) | Preparation system of laminated core rod | |
| TW201924548A (en) | Tobacco smoke filter | |
| CN119184347A (en) | Aerosol-generating article comprising an ordered aerosol-generating substrate of paper-based smoking filaments and method of making the same | |
| CN217509868U (en) | Outer cavity filter rod that inner core was filled | |
| CN121286763A (en) | A flavor-enhanced heated non-combustible cigarette and its preparation method | |
| CN119054949A (en) | A method for preparing a granular aerosol-generating product with hollow ends |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20230927 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20240417 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: A24D 3/02 20060101ALI20240411BHEP Ipc: A24D 3/04 20060101AFI20240411BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| INTG | Intention to grant announced |
Effective date: 20240607 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Free format text: CASE NUMBER: APP_38104/2024 Effective date: 20240626 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC ME MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602023000434 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241121 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1714588 Country of ref document: AT Kind code of ref document: T Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241122 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241223 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241221 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241121 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241121 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241223 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241121 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241221 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241122 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602023000434 Country of ref document: DE |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20250522 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250310 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20250331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250310 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20260318 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20240821 |