EP4112522B1 - Reel side yarn suction nozzle and winding machine provided with said reel side yarn suction nozzle - Google Patents
Reel side yarn suction nozzle and winding machine provided with said reel side yarn suction nozzle Download PDFInfo
- Publication number
- EP4112522B1 EP4112522B1 EP22173698.6A EP22173698A EP4112522B1 EP 4112522 B1 EP4112522 B1 EP 4112522B1 EP 22173698 A EP22173698 A EP 22173698A EP 4112522 B1 EP4112522 B1 EP 4112522B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- reel
- suction nozzle
- reel side
- side yarn
- comb
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H54/00—Winding, coiling, or depositing filamentary material
- B65H54/02—Winding and traversing material on to reels, bobbins, tubes, or like package cores or formers
- B65H54/40—Arrangements for rotating packages
- B65H54/44—Arrangements for rotating packages in which the package, core, or former is engaged with, or secured to, a driven member rotatable about the axis of the package
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H67/00—Replacing or removing cores, receptacles, or completed packages at paying-out, winding, or depositing stations
- B65H67/08—Automatic end-finding and material-interconnecting arrangements
- B65H67/081—Automatic end-finding and material-interconnecting arrangements acting after interruption of the winding process, e.g. yarn breakage, yarn cut or package replacement
- B65H67/085—Automatic end-finding and material-interconnecting arrangements acting after interruption of the winding process, e.g. yarn breakage, yarn cut or package replacement end-finding at the take-up package, e.g. by suction and reverse package rotation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H63/00—Warning or safety devices, e.g. automatic fault detectors, stop-motions ; Quality control of the package
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H71/00—Moistening, sizing, oiling, waxing, colouring or drying filamentary material as additional measures during package formation
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65H—HANDLING THIN OR FILAMENTARY MATERIAL, e.g. SHEETS, WEBS, CABLES
- B65H2701/00—Handled material; Storage means
- B65H2701/30—Handled filamentary material
- B65H2701/31—Textiles threads or artificial strands of filaments
Definitions
- the present invention relates to a reel side yarn suction nozzle and to a winding machine provided with said reel side yarn suction nozzle.
- thread or single thread or continuous thread refers to a single filament or continuous filament (for example in the case of silk, artificial or synthetic fibres), while the term yarn refers to a group of fibrils of varying lengths that are paralleled and joined together by twisting.
- thread or single thread or continuous thread refers to a single filament or continuous filament (for example in the case of silk, artificial or synthetic fibres)
- yarn refers to a group of fibrils of varying lengths that are paralleled and joined together by twisting.
- one or the other term will be used indifferently, it being understood that the applications of the present invention are not limited to one or the other type.
- the yarn produced by the spinning machine and wound into bobbins is unwound by special unravelling means, subjected to quality control by a sensor (yarn cleaner) and rewound by special winding means (cylinder) to form a reel.
- the yarn cleaner interrupts the winding by cutting the yarn, thus generating two ends, respectively bobbin side and reel side.
- the joining cycle the aim of which is to remove the defect from the reel and to intercept the two ends so as to position them inside the yarn joiner, which recreates the continuity of the yarn before resuming the winding process.
- the interception of the free yarn ends is carried out by two dedicated suction nozzles (usually called bobbin side yarn nozzle and reel side yarn nozzle) connected to a device that generates the necessary vacuum to achieve the flow conditions required to pick up the two yarns.
- the winding cylinder which normally rotates the reel so as to allow the yarn to be wound onto the reel, reverses its rotation in order to bring the free end in the direction of the reel and thus allow the reel side yarn nozzle to suck it in.
- a reel side yarn nozzle which, when connected to a suitable suction device, generates an air flow that favours the lifting of the yarn end in adherence to the surface of the reel is known.
- the input section of such a suction nozzle has a suitably shaped and tapered geometry such as to achieve at local level a high-speed flow along the entire width of the reel, measured parallel to the axis of rotation of the tube on which the reel is wound.
- the winding unit has to repeat the suction cycle several times due to failure to pick up the yarn end, thus decreasing the efficiency of the unit itself and therefore the productivity of the entire machine.
- Another known technique is the use of special combs, positioned inside the suction nozzle, in direct proximity to the input section thereof, which favour the retention and therefore the gripping of the yarn end.
- reference numeral 4 globally denotes a reel side yarn suction nozzle.
- said reel side yarn suction nozzle 4 is applied to a winding machine 8 comprising at least one winding unit having a reel 12 in formation.
- the reel 12 in formation is obtained by winding the yarn around a relative tube 16, in a known manner.
- the yarn produced and wound into bobbins is unwound by means of special unravelling means, subjected to quality control by a sensor (yarn cleaner) and rewound by special winding means (cylinder 20) to form the reel 12.
- the yarn cleaner interrupts the winding by cutting the yarn thus generating two ends, respectively the bobbin side yarn end (not illustrated)and reel side yarn end 24.
- it is first necessary to recover the yarn ends and then join them using a special yarn-joiner.
- the reel side yarn end 24 is intercepted by the reel side yarn suction nozzle 4 comprising an arm 28 movable from at least one rest position to at least one working or suction position. In the rest position, the arm 28 is in a distanced position or in any case not close to the reel 12, while in the working position the arm 28 is juxtaposed with the reel 12 in order to be able to intercept the reel side yarn end 24.
- the winding machine 8 is provided with drive means (not illustrated) for controlling the juxtaposition and distancing of the arm 28 with respect to the winding machine 12 in formation, as further described below.
- the arm 28 is fluidically connected to a suction source (not shown) to create a flow of suction air having a propagation direction X-X.
- the arm 28 terminates with a suction slit 32 having a rectilinear configuration elongated along a transverse direction T-T.
- the suction slit 32 with respect to a cross-section plane perpendicular to a first axis of rotation of the associable reel R1 and to a second axis of rotation R2 of the movable arm 28, has an upper lip 36 and a lower lip 40.
- the upper lip 36 is in a higher position, i.e., further to the side and facing the reel 12, when the arm 28 is brought into the working position. In the resting condition, the arm 28 may be rotated so as to reverse the positions of the lips.
- said upper lip 36 is set back from said lower lip 40, with respect to a propagation direction X-X of the suction air flow through the suction slit to the reel.
- the suction slit 32 has a transverse extension L, measured parallel to the transverse direction T-T, which is greater than or equal to the transverse extension of the reel 12, measured parallel to the axis of rotation of the reel R1.
- said suction slit 32 is provided with a deflector 44 and a comb 48.
- deflector 44 and the comb 48 are present together on the reel side yarn suction nozzle 4.
- the deflector 44 is oriented so as to induce a pinch of the air flow generated between the associated reel 12 and the suction slit 32, accelerating the air current and thereby facilitating the gripping of the free end of the yarn on the reel side 24.
- the deflector 44 and the comb 48 are arranged at the upper lip 36 of the suction slit 32.
- the deflector 44 and the comb 48 are arranged on opposite sides with respect to the upper lip 36; in particular, the deflector 44 faces opposite the lower lip 40, i.e., upwards when the arm 28 is in the working position, and the comb 48 faces the lower lip 40, i.e., downwards, when the arm 28 is in the working position.
- the deflector 44 and the comb 48 are arranged substantially aligned and adjacent to each other.
- the deflector 44 comprises a plate 56 having side ends provided with chamfered walls 60, i.e. inclined at an angle ⁇ ) of between 20° and 40°, preferably 30°, with respect to said transverse direction T-T.
- said chamfered walls 60 are connected with a connecting radius R of between 1 and 5 mm, preferably 3 mm, such as to prevent tangles of yarn ends at the deflector.
- the comb 48 comprises a roughened surface 64 so as to more easily retain the false yarn ends of the reel 12 before they enter the suction slit 32, so as to allow only the free yarn end to be intercepted by the comb 48.
- the comb 48 comprises a roughened surface 64 obtained by a surface roughening treatment, such as plasma treatment, at a portion of the comb 48 opposite the suction slit 32 and facing the reel 12.
- a surface roughening treatment such as plasma treatment
- the roughened surface 64 of the comb 48 has a roughness Ra of between 3 ⁇ m and 20 um.
- the roughened surface 64 has an isotropic roughness profile; in other words, no preferred direction of extension of the roughness grooves can be identified, as is the case, for example, with parallel or cross knurling.
- the roughened surface 64 extends along the entire transverse width of the comb 48, parallel to the transverse direction T-T, so as to cover the entire transverse extension of the reel 12.
- the winding machine 8 is provided with a processing and control unit (not illustrated) operatively connected to said drive means and programmed so that, during the suction phase of the reel side yarn end 24, the drive means bring the deflector 44 to a distance d from the lateral surface 52 of the reel 12 of between 1 mm and 5 mm, preferably 3 mm.
- the control of the arm position 28 by the processing and control unit may take place, for example, with the aid of an optical encoder.
- the diameter of the reel 12 in formation being known, it is possible to manage the positioning of the reel side yarn suction nozzle 4 with respect to the reel 12 so as to ensure a predetermined distance d of the deflector 44 from the lateral surface 52 of the reel 12.
- both the deflector and the comb contribute to resolving the technical problem of the present invention, since they improve the catching efficiency of the reel side yarn end.
- the deflector improves the suction capacity of the nozzle, while the rough surface of the comb makes it easier to retain the suctioned false yarn ends of the reel before they enter the suction slit, so that only the free yarn end can be intercepted by the comb.
- the two elements i.e. the deflector and the comb, cooperate synergistically with each other since the increase in the suction capacity of the suction slit enables the rough surface to better retain the false yarn ends.
Landscapes
- Engineering & Computer Science (AREA)
- Quality & Reliability (AREA)
- Textile Engineering (AREA)
- Replacing, Conveying, And Pick-Finding For Filamentary Materials (AREA)
- Spinning Methods And Devices For Manufacturing Artificial Fibers (AREA)
- Spinning Or Twisting Of Yarns (AREA)
Description
- The present invention relates to a reel side yarn suction nozzle and to a winding machine provided with said reel side yarn suction nozzle.
- It should be noted that the term thread or single thread or continuous thread refers to a single filament or continuous filament (for example in the case of silk, artificial or synthetic fibres), while the term yarn refers to a group of fibrils of varying lengths that are paralleled and joined together by twisting. Hereinafter, one or the other term will be used indifferently, it being understood that the applications of the present invention are not limited to one or the other type.
- As is known, in automatic winding machines the yarn produced by the spinning machine and wound into bobbins is unwound by special unravelling means, subjected to quality control by a sensor (yarn cleaner) and rewound by special winding means (cylinder) to form a reel. In particular, if during the winding of the bobbin yarn the characteristic parameters of the yarn are not acceptable, the yarn cleaner interrupts the winding by cutting the yarn, thus generating two ends, respectively bobbin side and reel side. This is followed by the joining cycle, the aim of which is to remove the defect from the reel and to intercept the two ends so as to position them inside the yarn joiner, which recreates the continuity of the yarn before resuming the winding process.
- The interception of the free yarn ends is carried out by two dedicated suction nozzles (usually called bobbin side yarn nozzle and reel side yarn nozzle) connected to a device that generates the necessary vacuum to achieve the flow conditions required to pick up the two yarns. In particular, after the yarn has been cut by the yarn cleaner, the winding cylinder, which normally rotates the reel so as to allow the yarn to be wound onto the reel, reverses its rotation in order to bring the free end in the direction of the reel and thus allow the reel side yarn nozzle to suck it in.
- In this context, the issue of having to pick up the reel side yarn end arises. Picking up the yarn end is, in fact, particularly problematic, since very often the yarn tends to adhere with extreme ease to the surface of the reel or to twist following the cut made by the yarn cleaner, crossing with other loops or arranging itself in a configuration not optimal for suction by the suction nozzle.
- The use of a reel side yarn nozzle which, when connected to a suitable suction device, generates an air flow that favours the lifting of the yarn end in adherence to the surface of the reel is known. Typically, the input section of such a suction nozzle has a suitably shaped and tapered geometry such as to achieve at local level a high-speed flow along the entire width of the reel, measured parallel to the axis of rotation of the tube on which the reel is wound.
- Often, however, the winding unit has to repeat the suction cycle several times due to failure to pick up the yarn end, thus decreasing the efficiency of the unit itself and therefore the productivity of the entire machine.
- Another known technique is the use of special combs, positioned inside the suction nozzle, in direct proximity to the input section thereof, which favour the retention and therefore the gripping of the yarn end.
- Compared to the nozzle without combs, this solution generally guarantees greater efficiency, but also typically requires operating at a greater distance from the reel in order to prevent so-called "loose loops", i.e. false yarn ends consisting of winding loops that have loosened due to imperfect adherence to the surface of the reel, from being sucked in together with the yarn end. Solutions according to prior art are disclosed, for example, by
EP 2574580 A2 andJP H0451476 U - The need is therefore felt to resolve the drawbacks and limitations mentioned with reference to the prior art.
- Such requirement is achieved by a winder according to claim 1,
- Further characteristics and advantages of the present invention will be more clearly comprehensible from the description given below of its preferred and non-limiting embodiments, wherein:
-
figure 1 shows a perspective view of a reel side yarn suction nozzle according to one embodiment of the present invention; -
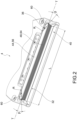
figure 2 shows a perspective view of the enlarged detail II shown infigure 1 ; -
figure 3 shows a schematic side view of a winding machine comprising a reel side yarn suction nozzle according to one embodiment of the present invention, during an initial phase of reel formation; -
figure 4 shows the enlarged detail IV shown infigure 3 ; -
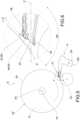
figure 5 shows a schematic side view of a winding machine comprising a reel side yarn suction nozzle according to one embodiment of the present invention, during a final phase of reel formation; -
figure 6 represents the enlarged detail VI shown infigure 5 . - The elements or parts of elements common to the embodiments described below will be indicated using the same reference numerals.
- With reference to the aforementioned figures,
reference numeral 4 globally denotes a reel side yarn suction nozzle. - Generally, said reel side
yarn suction nozzle 4 is applied to awinding machine 8 comprising at least one winding unit having areel 12 in formation. - The
reel 12 in formation is obtained by winding the yarn around arelative tube 16, in a known manner. - As seen in the introduction, the yarn produced and wound into bobbins is unwound by means of special unravelling means, subjected to quality control by a sensor (yarn cleaner) and rewound by special winding means (cylinder 20) to form the
reel 12. If, during the winding of the bobbin yarn the characteristic parameters of the yarn are not acceptable, the yarn cleaner interrupts the winding by cutting the yarn thus generating two ends, respectively the bobbin side yarn end (not illustrated)and reelside yarn end 24. In order to restore the continuity of the yarn, it is first necessary to recover the yarn ends and then join them using a special yarn-joiner. - The reel
side yarn end 24 is intercepted by the reel sideyarn suction nozzle 4 comprising anarm 28 movable from at least one rest position to at least one working or suction position. In the rest position, thearm 28 is in a distanced position or in any case not close to thereel 12, while in the working position thearm 28 is juxtaposed with thereel 12 in order to be able to intercept the reelside yarn end 24. - The
winding machine 8 is provided with drive means (not illustrated) for controlling the juxtaposition and distancing of thearm 28 with respect to thewinding machine 12 in formation, as further described below. - The
arm 28 is fluidically connected to a suction source (not shown) to create a flow of suction air having a propagation direction X-X. - The
arm 28 terminates with asuction slit 32 having a rectilinear configuration elongated along a transverse direction T-T. - The suction slit 32, with respect to a cross-section plane perpendicular to a first axis of rotation of the associable reel R1 and to a second axis of rotation R2 of the
movable arm 28, has anupper lip 36 and alower lip 40. - It should be noted that the
upper lip 36 is in a higher position, i.e., further to the side and facing thereel 12, when thearm 28 is brought into the working position. In the resting condition, thearm 28 may be rotated so as to reverse the positions of the lips. - According to a possible embodiment, said
upper lip 36 is set back from saidlower lip 40, with respect to a propagation direction X-X of the suction air flow through the suction slit to the reel. - Preferably, the
suction slit 32 has a transverse extension L, measured parallel to the transverse direction T-T, which is greater than or equal to the transverse extension of thereel 12, measured parallel to the axis of rotation of the reel R1. - According to the present invention said
suction slit 32 is provided with a deflector 44 and a comb 48. - It should be noted that the deflector 44 and the comb 48 are present together on the reel side
yarn suction nozzle 4. - Their co-presence certainly leads to a synergistic effect in terms of improved gripping capacity of the reel
side yarn end 24. - Preferably, the deflector 44 is oriented so as to induce a pinch of the air flow generated between the associated
reel 12 and thesuction slit 32, accelerating the air current and thereby facilitating the gripping of the free end of the yarn on thereel side 24. - According to one embodiment, the deflector 44 and the comb 48 are arranged at the
upper lip 36 of thesuction slit 32. - According to one embodiment, the deflector 44 and the comb 48 are arranged on opposite sides with respect to the
upper lip 36; in particular, the deflector 44 faces opposite thelower lip 40, i.e., upwards when thearm 28 is in the working position, and the comb 48 faces thelower lip 40, i.e., downwards, when thearm 28 is in the working position. - According to a possible embodiment, the deflector 44 and the comb 48 are arranged substantially aligned and adjacent to each other.
- According to one embodiment, the deflector 44 comprises a plate 56 having side ends provided with
chamfered walls 60, i.e. inclined at an angle β) of between 20° and 40°, preferably 30°, with respect to said transverse direction T-T. - For example, said
chamfered walls 60 are connected with a connecting radius R of between 1 and 5 mm, preferably 3 mm, such as to prevent tangles of yarn ends at the deflector. - The comb 48 comprises a roughened surface 64 so as to more easily retain the false yarn ends of the
reel 12 before they enter thesuction slit 32, so as to allow only the free yarn end to be intercepted by the comb 48. - For example, the comb 48 comprises a roughened surface 64 obtained by a surface roughening treatment, such as plasma treatment, at a portion of the comb 48 opposite the
suction slit 32 and facing thereel 12. - According to one embodiment, the roughened surface 64 of the comb 48 has a roughness Ra of between 3 µm and 20 um.
- According to one embodiment, the roughened surface 64 has an isotropic roughness profile; in other words, no preferred direction of extension of the roughness grooves can be identified, as is the case, for example, with parallel or cross knurling.
- According to a possible embodiment, the roughened surface 64 extends along the entire transverse width of the comb 48, parallel to the transverse direction T-T, so as to cover the entire transverse extension of the
reel 12. - According to a possible embodiment, the
winding machine 8 is provided with a processing and control unit (not illustrated) operatively connected to said drive means and programmed so that, during the suction phase of the reelside yarn end 24, the drive means bring the deflector 44 to a distance d from thelateral surface 52 of thereel 12 of between 1 mm and 5 mm, preferably 3 mm. - The control of the
arm position 28 by the processing and control unit may take place, for example, with the aid of an optical encoder. The diameter of thereel 12 in formation being known, it is possible to manage the positioning of the reel sideyarn suction nozzle 4 with respect to thereel 12 so as to ensure a predetermined distance d of the deflector 44 from thelateral surface 52 of thereel 12. - As may be appreciated from the description, the treatment method described above makes it possible to overcome the drawbacks of the prior art.
- First of all, the main advantages of the invention, appreciable especially in the case of particularly "slippery" yarns (such as, for example, viscose, polyester, blends) and/or fine count yarns, are as follows:
- reduction of the winding cycle time due to the shorter suction time needed to catch the yarn end;
- consequent increase in head efficiency and therefore in the productivity of the winder;
- increase in the quality of the yarn wound on the reel associated with a reduction in the number of cases in which the reel windings are disturbed;
- reduction of the possibility of single head alarms due mainly to loose loops tangled together due to repeated attempts to pick up the yarn end;
- consequently fewer stoppages in production processes following winding (warping, knitting, etc.) linked to the formation quality of the reel.
- It is to be noted that both the deflector and the comb contribute to resolving the technical problem of the present invention, since they improve the catching efficiency of the reel side yarn end.
- In fact, the deflector improves the suction capacity of the nozzle, while the rough surface of the comb makes it easier to retain the suctioned false yarn ends of the reel before they enter the suction slit, so that only the free yarn end can be intercepted by the comb.
- The two elements, i.e. the deflector and the comb, cooperate synergistically with each other since the increase in the suction capacity of the suction slit enables the rough surface to better retain the false yarn ends.
- A person skilled in the art may make numerous modifications and variations to the solutions described above so as to satisfy contingent and specific requirements.
- The scope of protection of the present invention is defined by the following claims.
Claims (12)
- A reel side yarn suction nozzle (4) comprising:- an arm (28) movable from at least one rest position to at least one working or suction position, the arm (28) being fluidly connected to a suction source to create a suction airflow,- the arm (28) terminating with a suction slit (32) having a rectilinear configuration elongated along a transverse direction (T-T), the suction slit (32), with respect to a cross-section plane perpendicular to a first axis of rotation (R1) of the associable reel (12) and to a second axis of rotation (R2) of the movable arm (28), has an upper lip (36) and a lower lip (40),- characterized in that said suction slit (32) is provided with a deflector (44) and a comb (48),- wherein the deflector (44) is oriented so as to induce a pinch of the air flow generated between the associated reel (12) and the suction slit (32), accelerating the air current and thereby facilitating the gripping of the free end of the yarn on the reel side (24),- wherein said comb (48) comprises a roughened surface (64) .
- The reel side yarn suction nozzle (4) according to claim 1, wherein said deflector (44) and said comb (48) are arranged at the upper lip (36) of the suction slit (32).
- The reel side yarn suction nozzle (4) according to claim 1 or 2, wherein the deflector (44) and the comb (48) are arranged on opposite sides of the upper lip (36), the deflector (44) facing opposite the lower lip (40) and the comb (48) facing the lower lip (40).
- The reel side yarn suction nozzle (4) according to any of the claims from 1 to 3, wherein the deflector (44) and the comb (48) are arranged substantially aligned and adjacent with each other.
- The reel side yarn suction nozzle (4) according to any of the claims from 1 to 4, wherein said upper lip (36) is set back from said lower lip (40), with respect to a propagation direction (X-X) of the suction air flow through the suction slit (32).
- The reel side yarn suction nozzle (4) according to any of the claims from 1 to 5, wherein the deflector (44) comprises a plate having side ends provided with chamfered walls (60), i.e. inclined at an angle (β) of between 20° and 40°, preferably 30°, with respect to said transverse direction (T-T).
- The reel side yarn suction nozzle (4) according to claim 6, wherein said chamfered walls (60) are connected with a connecting radius R of between 1 and 5 mm, preferably 3 mm, such as to prevent tangles of yarn ends at the deflector (44).
- The reel side yarn suction nozzle (4) according to any of the claims from 1 to 7, wherein said comb (48) comprises a roughened surface (64) obtained by means of a surface roughening treatment, at a portion of the comb (48) opposite the suction slit (32) and facing the reel (12) .
- The reel side yarn suction nozzle (4) according to claim 8, wherein the roughened surface (64) of the comb (48) has a roughness Ra between 3 µm and 20 µm.
- The reel side yarn suction nozzle (4) according to any of the claims from 8 to 9, wherein said roughened surface (64) has an isotropic roughness profile.
- The reel side yarn suction nozzle (4) according to any of the claims from 8 to 10, wherein the roughened surface (64) extends along the entire transverse width of the comb (48), parallel to the transverse direction (T-T) .
- A winding machine (8) comprising at least one winding unit having a reel (12) in formation and a reel side yarn suction nozzle(4) according to any of the claims from 1 to 11, and drive means for controlling the juxtaposition and distancing of the reel side yarn suction nozzle (4) with respect to the reel (12) in formation, wherein the winding machine (8) is provided with a processing and control unit operatively connected to said drive means and programmed so that, when suctioning the reel side yarn end (24), the drive means bring the deflector (44) to a distance d from the lateral surface (52) of the reel (12) of between 1 mm and 5 mm, preferably 3 mm.
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT102021000016862A IT202100016862A1 (en) | 2021-06-28 | 2021-06-28 | WIRE SUCTION NOZZLE ON THE PACKAGE SIDE AND RELATIVE WINDER EQUIPPED WITH THE SAID WIRE SUCTION NOZZLE ON THE PACKAGE SIDE |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP4112522A1 EP4112522A1 (en) | 2023-01-04 |
| EP4112522B1 true EP4112522B1 (en) | 2024-10-02 |
Family
ID=77627418
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP22173698.6A Active EP4112522B1 (en) | 2021-06-28 | 2022-05-17 | Reel side yarn suction nozzle and winding machine provided with said reel side yarn suction nozzle |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4112522B1 (en) |
| CN (2) | CN217920800U (en) |
| IT (1) | IT202100016862A1 (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| IT202100016862A1 (en) * | 2021-06-28 | 2022-12-28 | Savio Macch Tessili Spa | WIRE SUCTION NOZZLE ON THE PACKAGE SIDE AND RELATIVE WINDER EQUIPPED WITH THE SAID WIRE SUCTION NOZZLE ON THE PACKAGE SIDE |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH334274A (en) * | 1953-11-03 | 1958-11-30 | Reiners Walter Dr Ing | Suction nozzle for detecting, locating and lifting thread ends on a machine processing yarn, e.g. B. a winding machine |
| US2857113A (en) * | 1953-11-03 | 1958-10-21 | Reiners Walter Dr Ing | Suction nozzle for catching thread ends |
| JPS59173664U (en) * | 1983-05-04 | 1984-11-20 | 村田機械株式会社 | Packaging yarn end suction and holding device in yarn winding machine |
| GB2143548A (en) * | 1983-07-21 | 1985-02-13 | Hollingsworth | Yarn end catching |
| JPH0451476U (en) * | 1990-09-07 | 1992-04-30 | ||
| JPH0649457U (en) * | 1992-12-16 | 1994-07-08 | 東レエンジニアリング株式会社 | Suction mouse |
| JP4147432B2 (en) * | 2006-07-28 | 2008-09-10 | 村田機械株式会社 | Thread end drawing device |
| DE102011114765A1 (en) * | 2011-10-01 | 2013-04-04 | Oerlikon Textile Gmbh & Co. Kg | Comb strip for a suction nozzle of a workstation of a cheese-producing textile machine |
| DE102013011664A1 (en) * | 2013-07-11 | 2015-01-15 | Saurer Germany Gmbh & Co. Kg | Workplace of a cheese-producing textile machine |
| JP2015044685A (en) * | 2013-08-29 | 2015-03-12 | 村田機械株式会社 | Yarn end capturing device and yarn winding device |
| DE102015005393A1 (en) * | 2015-04-28 | 2016-11-03 | Saurer Germany Gmbh & Co. Kg | Workplace of a package winding textile machine |
| IT202100016862A1 (en) * | 2021-06-28 | 2022-12-28 | Savio Macch Tessili Spa | WIRE SUCTION NOZZLE ON THE PACKAGE SIDE AND RELATIVE WINDER EQUIPPED WITH THE SAID WIRE SUCTION NOZZLE ON THE PACKAGE SIDE |
-
2021
- 2021-06-28 IT IT102021000016862A patent/IT202100016862A1/en unknown
-
2022
- 2022-05-17 EP EP22173698.6A patent/EP4112522B1/en active Active
- 2022-05-27 CN CN202221310209.4U patent/CN217920800U/en active Active
- 2022-05-27 CN CN202210587827.1A patent/CN115594018A/en active Pending
Also Published As
| Publication number | Publication date |
|---|---|
| IT202100016862A1 (en) | 2022-12-28 |
| CN217920800U (en) | 2022-11-29 |
| EP4112522A1 (en) | 2023-01-04 |
| CN115594018A (en) | 2023-01-13 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| JP4082930B2 (en) | Yarn twisting device | |
| ITMI950463A1 (en) | DEVICE FOR PREPARING THE ENDS OF THE WIRES FOR TEXTILE MACHINES PRODUCING CROSSED SPOOLS | |
| CN106319698B (en) | A method for a spinning zone in a spinning frame and a spinning zone in a spinning frame | |
| ITMI951657A1 (en) | SERVICE DEVICE FOR A TEXTILE MACHINE PRODUCING CROSSED REELS | |
| EP4112522A1 (en) | Reel side yarn suction nozzle and winding machine provided with said reel side yarn suction nozzle | |
| JP2017082375A (en) | Work station operating method and work station | |
| Gandhi | Yarn preparation for weaving: winding | |
| CN108069291B (en) | Method, device and spinning winder for depositing yarn ends on bobbins | |
| EP1712504B1 (en) | Device and process for the handling and control of the yarn in a crosswinding head of a crosswinding machine in bobbin doffing operations | |
| CN110387615A (en) | Thread end suction device and method for thread end splicing unit | |
| EP1616829B1 (en) | Yarn guide device of revolving type automatic winder | |
| EP4074639B1 (en) | Winding machine with improved motorized yarn end extension lever and relative method of controlling the position of the yarn end extension lever | |
| US20250128906A1 (en) | Thread-guiding device for a workstation of a textile machine which produces cross-wound bobbins | |
| EP2574580B1 (en) | Comb bar for a suction nozzle for a workstation of a textile machine for creating cross-wound spools | |
| US4090676A (en) | Yarn or thread guiding device | |
| CN114852789B (en) | Method for operating a workstation of a spinning machine and workstation | |
| US10400362B2 (en) | Method for depositing a yarn end on a bobbin in a defined manner, a device and a spinning and winding machine for performing the method | |
| US10577728B2 (en) | Method for preparing a workstation for resumption of the spinning process on an air-jet spinning machine, and an air-jet spinning machine for performing the method | |
| CN106400216A (en) | A method of spinning yarn at the workstation of a rotor spinning machine and a device for its implementation | |
| CN105314462A (en) | Method and device for controlling the negative pressure on a thread catching or cleaning nozzle of a workstation of a textile machine | |
| CN113213275A (en) | Method for operating a workstation of a textile machine for producing bobbins | |
| CN111747233A (en) | Method for producing a piecing connection at a textile machine station and textile machine station | |
| CN115595700A (en) | Warping device and method for producing partial warps in yarn sheet | |
| CN115676499A (en) | Method for operating a workstation of a textile machine and a workstation of a textile machine | |
| JPS6221708B2 (en) |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20230328 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230526 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20240625 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602022006458 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20241002 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1728331 Country of ref document: AT Kind code of ref document: T Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250203 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250202 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250103 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250102 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602022006458 Country of ref document: DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250523 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20250512 Year of fee payment: 4 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| 26N | No opposition filed |
Effective date: 20250703 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: H13 Free format text: ST27 STATUS EVENT CODE: U-0-0-H10-H13 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20251223 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250517 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250531 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20250531 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241002 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250517 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250531 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20260306 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250531 |