EP3171109B1 - Optimization of nucleation and crystallization for lyophilization using gap freezing - Google Patents
Optimization of nucleation and crystallization for lyophilization using gap freezing Download PDFInfo
- Publication number
- EP3171109B1 EP3171109B1 EP16200274.5A EP16200274A EP3171109B1 EP 3171109 B1 EP3171109 B1 EP 3171109B1 EP 16200274 A EP16200274 A EP 16200274A EP 3171109 B1 EP3171109 B1 EP 3171109B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- heat sink
- container
- tray
- thermal conduction
- freezing
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
Images






Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F26—DRYING
- F26B—DRYING SOLID MATERIALS OR OBJECTS BY REMOVING LIQUID THEREFROM
- F26B5/00—Drying solid materials or objects by processes not involving the application of heat
- F26B5/04—Drying solid materials or objects by processes not involving the application of heat by evaporation or sublimation of moisture under reduced pressure, e.g. in a vacuum
- F26B5/06—Drying solid materials or objects by processes not involving the application of heat by evaporation or sublimation of moisture under reduced pressure, e.g. in a vacuum the process involving freezing
Definitions
- This disclosure relates to methods and apparatus used for lyophilizing liquid solutions of solutes.
- the disclosure provides a method for optimization of the nucleation and crystallization of the liquid solution during freezing to produce lyophilized cakes of the solutes with large, consistent pore sizes,
- the disclosure also provides a method for rapid lyophilization of the frozen liquid solution.
- the disclosure additionally provides apparatus for use with the method and lyophilization chambers.
- lyophilization involves the freeze-drying of solutes. Typically, a solution is loaded into a lyophilization chamber, the solution is frozen, and the frozen solvent is removed by sublimation under reduced pressure.
- US 4,953,299 describes a process and apparatus for freeze-drying, said apparatus comprising freeze-drying shelves disposed inside a freeze-drying enclosure, on which may be placed products or solutions to be freeze-dried.
- the product or solutions may be contained in open recipients, as well as cooling and/or heating means associated with and preferably incorporated in said shelves.
- the means forming a thermal shield are disposed between said freeze-drying shelves, thus making it possible to slow down the heat exchanges between the surface of the product to be freeze-dried and the heating and/or cooling elements associated with the shelves.
- DE 22 35 483 is concerned with a freeze drying apparatus configured to make better use of the available drying space when freeze drying plants to increase their drying capacity.
- WO 2012/054194 discloses devices, articles, and methods useful for producing lyophilized cakes of solutes.
- the devices and articles provide for a method of freezing liquid solutions of the solute by the top and the bottom of the solution simultaneously.
- the frozen solution then provides a lyophilized cake of the solutes with large and uniform pores.
- One well known issue associated with the lyophilization of materials is the formation of one or more layers of the solute (the dissolved materials) on the top of the frozen solution. These layers form during the freezing of the solution because, typically, the solutions are positioned within the lyophilization chamber on a heat sink which rapidly decreases in temperature and causes the solution to freeze from the bottom up. This bottom up freezing pushes the solute in the liquid phase closer to the top of the solution and increases the solute concentration in the still liquid solution. The high concentration of solute can then form a solid mass that can inhibit the flow of gasses therethrough. In a worse case, the solute forms an amorphous solid that is nearly impermeable and prevents sublimation of the frozen solvent. These layers of concentrated solute can inhibit the sublimation of the frozen solvent and may require use of higher drying temperatures and/or longer drying times.
- Disclosed herein is an apparatus for and method of freezing a material, e.g., for subsequent lyophilization, that can prevent the formation of these layers and thereby provide efficient sublimation of the frozen solvent.
- the lyophilization or freeze drying of solutes is the sublimation of frozen liquids, leaving a non-subliming material as a resultant product.
- the non-subliming material is generally referred to as a solute.
- a common lyophilization procedure involves loading a lyophilization chamber with a container that contains a liquid solution of at least one solute. The liquid solution is then frozen. After freezing, the pressure in the chamber is reduced sufficiently to sublime the frozen solvent, such as water, from the frozen solution.
- the lyophilization device or chamber is adapted for the freeze drying of samples in containers by including at least one tray for supporting the container and means for reducing the pressure in the chamber (e.g., a vacuum pump).
- a vacuum pump e.g., a vacuum pump.
- Many lyophilization devices and chambers are commercially available.
- the lyophilization chamber includes a heat sink 101 that facilitates the lowering of the temperature within the chamber.
- the heat sink 101 includes a heat sink surface 102 that is exposed to the internal volume of the lyophilization chamber and is in thermal communication with a refrigerant 103.
- the refrigerant 103 can be carried in the heat sink 101 within a refrigerant conduit 104.
- the refrigerant conduit 104 can carry the heat sink surface 102 or can be in fluid communication with the heat sink surface 102 for example through a heat sink medium 105.
- the heat sink medium 105 is a thermal conductor, not insulator, and preferably has a thermal conductivity of greater than about 0.25, 0.5, and/or 1 W/mK at 25 °C.
- the sample containers 106 do not sit on or in direct, substantial thermal conductivity with the heat sink 101 during freezing.
- the sample containers 106 sit on or are carried by a tray surface 107 that is thermally insulated from the heat sink 101.
- the sample containers 106 are thermally insulated by being suspended above the heat sink 101.
- the tray surface 107 is thermally insulated from the heat sink 101 by a thermal insulator 108.
- the thermal insulator 108 has a thermal conductivity of less than about 0.2, less than 0.1, and/or less than 0.05 W/mK at 25 °C.
- the thermal insulator 108 can be a gas, a partial or complete vacuum, a paper, a foam (e.g., a foam having flexibility at cryogenic temperatures), a polymeric material, or a combination or other mixture of thereof.
- the polymeric material can be free of or substantially free of open cells or can be a polymeric foam (e.g., a cured foam).
- the thermal insulator 108 refers to the material, object and/or space that provides thermal insulation from the heat sink 101. Air is still considered a thermal insulator in a method or apparatus wherein the pressure of the air is decreased due to evacuation of the lyophilization chamber.
- the level of thermal insulation provided by the thermal insulator 108 can be dependent on the thickness of the thermal insulator 108. This thickness can be measured by the distance 109 from the heat sink surface 102 to the tray surface 107, for example. This distance 109, limited by the internal size of the lyophilization chamber, can be in a range of about 0.5 to about 50 mm, for example, or smaller if the thermal isolation is very high. This distance 109 can be optimized for specific lyophilization chamber volumes and preferably is greater than about 0.5, 0.75, 1, 1.5, 2, 2.5, 3, 3.5, 4, 4.5, 5, 5.5, 6, 6.5, 7, 7.5, 8, 8.5, 9, 9.5, 10, 15, 20, 25, 30, 35, 40, 45, or 50 mm.
- the distance 109 can be larger than about 10 mm, the volume within the lyophilization device is typically better used by optimizing the distances below about 20 mm.
- the distance between the heat sink surface 102 and the tray surface 107 is only limited by the distance between the heat sink surface 102 and the upper heat sink 101 minus the height of a vial 106.
- the preferred distance 109 can be dependent on the specific model and condition of lyophilization chamber, heat sink, refrigerant, and the like, and is readily optimized by the person of ordinary skill in view of the present disclosure to avoid uneven freezing from top and bottom surfaces of the solution in the container.
- the tray surface 107 is carried by a tray 110, preferably a rigid tray.
- the tray surface 107 can be a thermal insulator (e.g., foamed polyurethane) or a thermal conductor (e.g., stainless steel).
- the thermal insulator 108 may comprise a gas, a partial vacuum, or a full vacuum.
- the tray 110 is preferably maintained at a fixed distance between heat sink surface 102 and the tray surface 107 during freezing.
- the tray 110 can be spaced from the heat sink surface 102 by the thermal insulator 108 formed in an embodiment to include a spacer 111 positioned between the tray 110 and the heat sink surface 102 or can be spaced from the heat sink surface 102 to form the thermal insulator 108 by operationally engaging the tray 110 to a bracket 112 affixed to an internal surface 113 (e.g., wall) of the lyophilization chamber.
- the tray 110 is maintained at a distance from the heat sink surface 102 to form the thermal insulator 108 by a plurality of struts (not shown) that operationally engage the tray 110 and heat sink surface 102.
- a spacer 111 supports the tray 110
- the distance from the heat sink surface 102 to the tray surface 107 is the thickness of the spacer 111 plus the thickness of the tray 110.
- the spacer 111 can have a thickness in a range of about 0.5 mm to about 10 mm, about 1 mm to about 9 mm, about 2 mm to about 8 mm, and/or about 3 mm to about 7 mm, for example.
- the tray 110 can be carried by one or more spacers 111 placed between the heat sink surface 102 and the tray 110.
- the tray 110 can be carried by the thermal insulator 108 comprising a rigid thermal insulator.
- the tray 110 can be a thermal conductor (e.g., stainless steel) and supported by (e.g., resting on) a thermal insulator (e.g., foamed polyurethane).
- the rigid thermal insulator can be combined with spacers to carry the tray.
- the rigid thermal insulator (with or without the spacer) can have a thickness in a range of about 0.5 mm to about 10 mm, about 1 mm to about 9 mm, about 2 mm to about 8 mm, and/or about 3 mm to about 7 mm, for example.
- the lyophilization device can include a plurality of heat sinks 101 that individually have a heat sink surface 102 in thermal communication with a refrigerant 103.
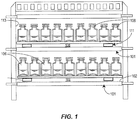
- the heat sinks 101 can be disposed vertically in the lyophilization chamber with respect to each other, forming upper and lower heat sinks 101 (see e.g., Figure 1 ).
- the lower heat sink surface 102 is disposed between the upper and lower heat sinks and the tray surface 107 is disposed between the upper heat sink 101 and the lower heat sink surface 102.
- the thermal insulator 108 is disposed between the tray surface 107 and the lower heat sink 101.
- each individual sample container 106 can sit on or be carried by a thermal insulator 108 (see e.g., Figure 4b ).
- the thermal insulator 108 can comprise a thermally insulating support 114 affixed to the bottom of the vial 115 (see e.g., Figure 4c ).
- the thermally insulating support 114 can have a thermal conductivity less than about 0.2 W/mK, less than about 0.1 W/mK, and/or less than about 0.05 W/mK at 25 °C, for example.
- the vial 106 and the insulating support 114 are different materials (e.g., the vial can comprise a glass and the insulating support can comprise a foam or a polymer).
- the vial can comprise a sealable vial.
- the invention is directed to a method of freezing a liquid solution for subsequent lyophilization.
- the lyophilization chamber as described above is loaded with a liquid solution held in a container that includes an active pharmaceutical agent solute and a solvent.
- the liquid solution will have a top surface 116 and a bottom surface, wherein the bottom surface 117 is proximal to the heat sink 101 (see Figure 5 ).
- the container is separated from the heat sink 101 by providing a thermal insulator 108 between the container and the heat sink 101, the thermal insulator having the characteristics described herein.
- the container is spaced vertically from the heat sink with an intervening thermal insulator 108, the distance and thermal insulator 108 being selected to provide freezing of the liquid solution from the top and bottom surfaces at approximately the same rate.
- the liquid solution can be frozen by lowering the temperature of the heat sink 101 and thereby the ambient temperature in the lyophilization chamber.
- the liquid solution advantageously can be frozen from the top and the bottom surfaces at approximately the same rate to form a frozen solution.
- a further advantage is that the concurrent water to ice conversion at the top and bottom of the solution avoids problematic freeze-concentration and skin formation observed when the bottom of the solution freezes more rapidly than the top.
- a further embodiment of the inventions includes once frozen, the liquid solution (now the frozen solution) can be lyophilized to yield a lyophilized cake.
- the solution is lyophilized without any significant change in the thermal insulator 108 such as by example maintaining the physical arrangement of the container and heat sink elements.
- the container having the frozen liquid solution is placed in thermally-conductive contact with the heat sink during or following freezing, for example by removing the thermal insulator 108 and placing the tray 107 or containers directly on the shelf.
- Embodiments of the removal can comprise, removing the spacer 111, moving the brackets 112 or altering the length of the struts (not shown).
- thermal insulator container not be placed in thermally conductive contact with the heat sink but the insulation characteristics of the thermal insulator 108 be altered such as by significantly lessening the insulation characteristics by reducing the spacing between the tray and heat sink to a minimal distance.
- thermal insulator 108 or portions thereof between one or more of the container and heat sink can dimensionally vary from the thermal insulator or portions thereof between one or more remaining containers.
- the thickness of the thermal insulator 108 can be reduced for edge and/or corner containers, relative to the thickness of the thermal insulator 108 between center containers and heat sink, in order to counter-balance the radiant heating experienced by such edge and corner containers from side walls and thus achieve more consistent temperature profiles across the array.
- the thermal insulator provides for the facile freezing of the liquid solution from the top and the bottom within the lyophilization chamber at approximately the same rate.
- the freezing of the liquid solution from the top and the bottom can be determined by measuring the temperature of the solution during the freezing process.
- the temperature can be measured by inserting at least two thermocouples into a vial containing the solution.
- a first thermocouple 118 can be positioned at the bottom of the solution, at about the center of the vial, for example, and a second thermocouple 119 can be positioned at the top of the solution, just below the surface of the solution, in about the center of the vial, for example.
- the thermal insulator e.g., type and thickness
- the thermal insulator can be selected to provide a water-ice conversion index value in a range of about -2 °C to about 2 °C, or about -1 °C to about 1 °C, and/or about -0.5 °C to about 0.5 °C.
- the water-ice conversion index is zero or a positive value.
- the water-ice conversion index is determined by a method including first plotting the temperatures reported by the thermocouples at the top (T t ) and at the bottom (T b ) of the solution as a function of time.
- the water-ice conversion index is the area between the curves, in °C•minute, between a first nucleation event and the end of water-ice conversion divided by the water-ice conversion time, in minutes.
- the water-ice conversion time is the time necessary for the temperature at the top (T t ) of the solution to reduce in value below the freezing point plateau for the solution.
- the temperature data are collected by loading solution-filled vials into a lyophilization chamber.
- the temperature can then be recorded until a time after which the top and the bottom of the solution cool to a temperature below the freezing point plateau.
- the areas, positive and negative, are measured from the first nucleation event (observable in the plot of temperatures, e.g., such as in Figure 6 ) 122 until both temperature values cool below the freezing point plateau 123.
- the sum of these areas provides the area between the curves.
- the value is positive when the temperature at the bottom of the vial (T b ) is warmer than the temperature at the top of the vial (T t ) 120 and the value is negative when the temperature at the top of the vial (T t ) is warmer than the temperature at the bottom of the vial (T b ) 121.
- the water-ice conversion index is zero or a positive value.
- the water-ice conversion index value in one type of embodiment will be in a range of about 0°C to about 2°C, or about 0°C to about 1°C, or about 0°C to about 0.5°C.
- the cooling rate, temperature of the tray, and the thermal insulator can be optimized to provide an area between the curves at or near 0 °C•minute.
- Figure 7 shows the water-ice conversion indices for 5 wt.% aqueous solutions of sucrose in vials on a stainless steel tray as a function of the distance from the heat sink surface to the stainless steel tray, with the thermal insulator 108 comprising air within a gap between the heat sink surface and the bottom of the stainless steel tray.
- the tray had a thickness of about 1.2 mm.
- Still another embodiment of the invention is a lyophilized cake made by a method disclosed herein.
- the lyophilized cake can include a substantially dry lyophilized material and a plurality of pores in the lyophilized material having substantially the same pore size.
- the lyophilized cake has a pore size that is substantially larger than the pore size of a reference lyophilized cake comprising the same material as the lyophilized cake but made by a standard lyophilization process (e.g., placing a vial 106 comprising a liquid solution onto a heat sink 101 within a lyophilization chamber, excluding a thermal insulator between the vial and the heat sink 101, lowering the temperature of the heat sink 101 and thereby freezing the liquid solution, and then lyophilizing the frozen solution).
- a standard lyophilization process e.g., placing a vial 106 comprising a liquid solution onto a heat sink 101 within a lyophilization chamber, excluding a thermal insulator between the vial
- the cross-sectional area of the cylindrical pores of the lyophilized cake is preferably at least 1.1, 2, and/or 3 times greater than the cross-sectional area of the reference lyophilized cake.
- the lyophilized cake has a substantially consistent pore size throughout the cake.
- the size of pores in the lyophilized cake can be measured by a BET surface area analyzer.
- the effective pore radius (r e ), a measure of the pore size, can be calculated from the measured surface area of the pores (SSA) by assuming cylindrical pores.
- the effective pore radius, r e was determined by a pore diffusion model. See Kuu et al. "Product Mass Transfer Resistance Directly Determined During Freeze-Drying Using Tunable Diode Laser Absorption Spectroscopy (TDLAS) and Pore Diffusion Model.” Pharm. Dev. Technol. (available online at: http://www.ncbi.nlm.nih.Qov/pubmed/20387998 and later published in Vol. 16, no. 4, p. 343-357, 2011 ). The results are presented in Figure 9 , where it can be seen that the pore radius of the cakes on the bottom shelf is much larger than that on the top shelf. The results demonstrate that the 6mm gapped tray is very effective for pore enlargement.
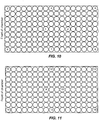
- thermocouples For monitoring the product temperature on each shelf, two thermocouples were placed in center vials and six thermocouples were placed on the edge locations of the shelves, as shown in Figures 10 and 11 , wherein the numbers indicate temperature-probed vials.
- the shelf temperature (each) was cooled to -70° C, followed by holding the shelf at -70°C for 90 minutes. At this low shelf temperature, cooling of vials can be accelerated, since cooling with a gap is primarily driven by radiation.
- the shelf was then heated to -50° C, followed by holding the shelf at -50°C for 60 minutes. After the solution was frozen the shelf temperature was raised to a higher temperature of -50°C because after complete freezing of the solution it is not necessary to maintain it at - 70oC for vacuum pulling. For one of the trays, the thermal insulator 108 was removed prior to vacuum pulling by removing the spacer.
- the lyophilization chamber was then evacuated to a set-point of 13332.2 mPa (100 mTorr), (b) the shelf temperature was held at -50°C (at 13332.2 mPa (100 mTorr)) for 30 minutes; (c) the shelf temperature was then ramped to -15°C (at 13332.2 mPa (100 mTorr)) at a rate of 0.5 °C/min; and (d) the shelf temperature was then held at -15°C (at 13332.2 mPa (100 mTorr)) until the end of primary drying.
- the shelf temperature was ramped to 30 °C (at 13332.2 mPa (100 mTorr)), at a rate of 0.5 °C/min; and (f) the shelf temperature was then held at 30 °C (at 13332.2 mPa (100 mTorr)) until the end of secondary drying.
- the product temperature profiles of the corner vials are not representative for a manufacturing scale freeze dryer due to the strong thermal radiation from the front and back walls to corner vials in this freeze dryer.
- the front wall of the LyoStarTM II freeze dryer is acrylic without insulation.
- the back wall of the chamber has insulation, but the large amount of heat produced by the fluid pump penetrates through the insulation and raises the product temperature to some extent.
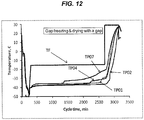
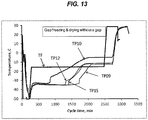
- Figs. 12 and 13 the drying time on the top shelf ( Fig. 12 , thermal insulator remaining during vacuum pulling) is much longer than that on the bottom shelf ( Fig. 13 , thermal insulator removed before vacuum pulling) due to the much higher heat transfer rate on the bottom shelf without a thermal insulator.
- Fig. 12 shows that after approximate 2670 minutes of cycle time, primary drying was still not complete, since the temperature in the center vial, TP02 did not move out of the plateau level during primary drying.
- Fig. 13 shows that after approximate 1690 minutes of cycle time, primary drying was complete, since the temperatures in the center vials, TP09 and TP10 moved out of the plateau levels of primary drying.
- Inlet temperatures of the shelf refrigerant fluids are plotted as Tf on each of Figures 12 and 13 .
- Fig. 15 The comparison is shown in Fig. 15 , in which the difference between TP02 and TP07 is about 1.5°C.
- the vials on the tray without a thermal insulator between the tray and shelf during drying are dried much faster than those with a thermal insulator between the tray and shelf during drying.
- the tray without a thermal insulator during drying also has the advantage of reducing the temperature difference between the center and edge vials, which could be important for some temperature-sensitive formulations.
Landscapes
- Engineering & Computer Science (AREA)
- Health & Medical Sciences (AREA)
- Life Sciences & Earth Sciences (AREA)
- Molecular Biology (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Drying Of Solid Materials (AREA)
- Bakery Products And Manufacturing Methods Therefor (AREA)
- Confectionery (AREA)
Description
- This disclosure relates to methods and apparatus used for lyophilizing liquid solutions of solutes. The disclosure provides a method for optimization of the nucleation and crystallization of the liquid solution during freezing to produce lyophilized cakes of the solutes with large, consistent pore sizes, The disclosure also provides a method for rapid lyophilization of the frozen liquid solution. The disclosure additionally provides apparatus for use with the method and lyophilization chambers.
- The preservation of materials encompasses a variety of methods. One important method, lyophilization, involves the freeze-drying of solutes. Typically, a solution is loaded into a lyophilization chamber, the solution is frozen, and the frozen solvent is removed by sublimation under reduced pressure.
- One well known issue associated with the lyophilization of materials (e.g., sugars) is the formation of one or more layers of the solute (the dissolved materials) on the top of the frozen solution. In a worse case, the solute forms an amorphous solid that is nearly impermeable and eventually prevents sublimation of the frozen solvent. These layers of concentrated solute can inhibit the sublimation of the frozen solvent and may require use of higher drying temperatures and/or longer drying times. The higher drying temperatures may negatively impact the integrity of the solute and the longer drying time may have a negative effect on the economics of the process.
-
US 4,953,299 describes a process and apparatus for freeze-drying, said apparatus comprising freeze-drying shelves disposed inside a freeze-drying enclosure, on which may be placed products or solutions to be freeze-dried. The product or solutions may be contained in open recipients, as well as cooling and/or heating means associated with and preferably incorporated in said shelves. The means forming a thermal shield are disposed between said freeze-drying shelves, thus making it possible to slow down the heat exchanges between the surface of the product to be freeze-dried and the heating and/or cooling elements associated with the shelves. -
DE 22 35 483 is concerned with a freeze drying apparatus configured to make better use of the available drying space when freeze drying plants to increase their drying capacity. -
WO 2012/054194 discloses devices, articles, and methods useful for producing lyophilized cakes of solutes. The devices and articles provide for a method of freezing liquid solutions of the solute by the top and the bottom of the solution simultaneously. The frozen solution then provides a lyophilized cake of the solutes with large and uniform pores. - The invention is set out in the appended claims.
- For a more complete understanding of the disclosure, reference should be made to the following detailed description and accompanying drawing figures wherein:
-
Figure 1 is a drawing of the inside of a lyophilization device showing a lyophilization chamber and a plurality of heat sinks in a vertical arrangement; -
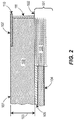
Figure 2 is a composite drawing of an article showing an arrangement of a heat sink surface and a tray surface; -
Figure 3 is another composite drawing of an article showing an arrangement of a plurality of heat sinks and the location and separation of the heat sink surface and the tray surface; -
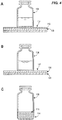
Figure 4 is illustrations of sample containers, here vials, (4a) positioned on a tray, (4b) positioned directly on a thermal insulator, or (4c) combined with a thermally insulating support; -
Figure 5 is a drawing of a sample vial including a liquid solution showing the placement of thermocouples useful for the measurement of the temperatures of the top and the bottom of the solution; -
Figure 6 is a plot of the temperatures of the top and the bottom of a 10 wt.% aqueous sucrose solution frozen using a 3mm gap between a heat sink surface and a tray (the tray having a thickness of about 1.2 mm) showing a nucleation event, the differences in temperatures between the top and the bottom of the solution, and the reduction in temperature of the top of the solution after the freezing point plateau; -
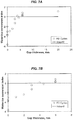
Figure 7 is plots of the water-ice conversion indices for a 5 wt. % aqueous sucrose solution as a function of distance (air gap) from a heat sink surface to a tray (the tray having a thickness of about 1.2 mm); -
Figure 8 is a plot of the internal temperatures of vials during a primary drying process illustrating the effect of gap-freezing on the product temperature during freeze-drying; -
Figure 9 is a plot of effective pore radii for samples frozen on a 6 mm gapped tray and samples frozen directly on the heat sink surface; -
Figures 10 and 11 are temperature probe diagrams for top shelf and bottom shelf vials according to Example 2; -
Figures 12 and13 are comparisons of approximate drying time for vials on the top shelf and bottom shelf, according to Example 2; -
Figure 14 is a comparison of product temperatures of top shelf center vials and bottom shelf center vials during drying, according to Example 2; -
Figure 15 is a comparison of product temperatures of top shelf center vials and edge vials TP04 and TP07 during drying, according to Example 2; and -
Figure 16 is a comparison of product temperatures of bottom shelf center vials and edge vials during drying, according to Example 2. - While the disclosed methods and articles are susceptible of embodiments in various forms, there are illustrated in the examples and figures (and will hereafter be described) specific embodiments of the methods and articles, with the understanding that the disclosure is intended to be illustrative, and is not intended to limit the invention to the specific embodiments described and illustrated herein.
- One well known issue associated with the lyophilization of materials (e.g., sugars) is the formation of one or more layers of the solute (the dissolved materials) on the top of the frozen solution. These layers form during the freezing of the solution because, typically, the solutions are positioned within the lyophilization chamber on a heat sink which rapidly decreases in temperature and causes the solution to freeze from the bottom up. This bottom up freezing pushes the solute in the liquid phase closer to the top of the solution and increases the solute concentration in the still liquid solution. The high concentration of solute can then form a solid mass that can inhibit the flow of gasses therethrough. In a worse case, the solute forms an amorphous solid that is nearly impermeable and prevents sublimation of the frozen solvent. These layers of concentrated solute can inhibit the sublimation of the frozen solvent and may require use of higher drying temperatures and/or longer drying times.
- Disclosed herein is an apparatus for and method of freezing a material, e.g., for subsequent lyophilization, that can prevent the formation of these layers and thereby provide efficient sublimation of the frozen solvent.
- The lyophilization or freeze drying of solutes is the sublimation of frozen liquids, leaving a non-subliming material as a resultant product. Herein, the non-subliming material is generally referred to as a solute. A common lyophilization procedure involves loading a lyophilization chamber with a container that contains a liquid solution of at least one solute. The liquid solution is then frozen. After freezing, the pressure in the chamber is reduced sufficiently to sublime the frozen solvent, such as water, from the frozen solution.
- The lyophilization device or chamber is adapted for the freeze drying of samples in containers by including at least one tray for supporting the container and means for reducing the pressure in the chamber (e.g., a vacuum pump). Many lyophilization devices and chambers are commercially available.
- With reference to
Figures 1-3 , the lyophilization chamber includes aheat sink 101 that facilitates the lowering of the temperature within the chamber. Theheat sink 101 includes aheat sink surface 102 that is exposed to the internal volume of the lyophilization chamber and is in thermal communication with arefrigerant 103. Therefrigerant 103 can be carried in theheat sink 101 within arefrigerant conduit 104. Therefrigerant conduit 104 can carry theheat sink surface 102 or can be in fluid communication with theheat sink surface 102 for example through aheat sink medium 105. Theheat sink medium 105 is a thermal conductor, not insulator, and preferably has a thermal conductivity of greater than about 0.25, 0.5, and/or 1 W/mK at 25 °C. - According to the novel method described herein, the
sample containers 106 do not sit on or in direct, substantial thermal conductivity with theheat sink 101 during freezing. In one embodiment, thesample containers 106 sit on or are carried by atray surface 107 that is thermally insulated from theheat sink 101. In another embodiment, thesample containers 106 are thermally insulated by being suspended above theheat sink 101. - The
tray surface 107 is thermally insulated from theheat sink 101 by athermal insulator 108. Thethermal insulator 108 has a thermal conductivity of less than about 0.2, less than 0.1, and/or less than 0.05 W/mK at 25 °C. Thethermal insulator 108 can be a gas, a partial or complete vacuum, a paper, a foam (e.g., a foam having flexibility at cryogenic temperatures), a polymeric material, or a combination or other mixture of thereof. The polymeric material can be free of or substantially free of open cells or can be a polymeric foam (e.g., a cured foam). As used herein, thethermal insulator 108 refers to the material, object and/or space that provides thermal insulation from theheat sink 101. Air is still considered a thermal insulator in a method or apparatus wherein the pressure of the air is decreased due to evacuation of the lyophilization chamber. - The level of thermal insulation provided by the
thermal insulator 108 can be dependent on the thickness of thethermal insulator 108. This thickness can be measured by thedistance 109 from theheat sink surface 102 to thetray surface 107, for example. Thisdistance 109, limited by the internal size of the lyophilization chamber, can be in a range of about 0.5 to about 50 mm, for example, or smaller if the thermal isolation is very high. Thisdistance 109 can be optimized for specific lyophilization chamber volumes and preferably is greater than about 0.5, 0.75, 1, 1.5, 2, 2.5, 3, 3.5, 4, 4.5, 5, 5.5, 6, 6.5, 7, 7.5, 8, 8.5, 9, 9.5, 10, 15, 20, 25, 30, 35, 40, 45, or 50 mm. While thedistance 109 can be larger than about 10 mm, the volume within the lyophilization device is typically better used by optimizing the distances below about 20 mm. Notably, the distance between theheat sink surface 102 and thetray surface 107 is only limited by the distance between theheat sink surface 102 and theupper heat sink 101 minus the height of avial 106. Thepreferred distance 109 can be dependent on the specific model and condition of lyophilization chamber, heat sink, refrigerant, and the like, and is readily optimized by the person of ordinary skill in view of the present disclosure to avoid uneven freezing from top and bottom surfaces of the solution in the container. - In an embodiment where the
tray surface 107 is thermally insulated from theheat sink 101, thetray surface 107 is carried by atray 110, preferably a rigid tray. Notably, thetray surface 107 can be a thermal insulator (e.g., foamed polyurethane) or a thermal conductor (e.g., stainless steel). In such an embodiment thethermal insulator 108 may comprise a gas, a partial vacuum, or a full vacuum. - The
tray 110 is preferably maintained at a fixed distance betweenheat sink surface 102 and thetray surface 107 during freezing. Thetray 110 can be spaced from theheat sink surface 102 by thethermal insulator 108 formed in an embodiment to include aspacer 111 positioned between thetray 110 and theheat sink surface 102 or can be spaced from theheat sink surface 102 to form thethermal insulator 108 by operationally engaging thetray 110 to abracket 112 affixed to an internal surface 113 (e.g., wall) of the lyophilization chamber. In a further embodiment, thetray 110 is maintained at a distance from theheat sink surface 102 to form thethermal insulator 108 by a plurality of struts (not shown) that operationally engage thetray 110 andheat sink surface 102. In an embodiment where aspacer 111 supports thetray 110, the distance from theheat sink surface 102 to thetray surface 107 is the thickness of thespacer 111 plus the thickness of thetray 110. In agreement with the distances disclosed above, thespacer 111 can have a thickness in a range of about 0.5 mm to about 10 mm, about 1 mm to about 9 mm, about 2 mm to about 8 mm, and/or about 3 mm to about 7 mm, for example. Thetray 110 can be carried by one ormore spacers 111 placed between theheat sink surface 102 and thetray 110. - In another embodiment, the
tray 110 can be carried by thethermal insulator 108 comprising a rigid thermal insulator. For example thetray 110 can be a thermal conductor (e.g., stainless steel) and supported by (e.g., resting on) a thermal insulator (e.g., foamed polyurethane). In a further embodiment the rigid thermal insulator can be combined with spacers to carry the tray. In agreement with the distances disclosed above, the rigid thermal insulator (with or without the spacer) can have a thickness in a range of about 0.5 mm to about 10 mm, about 1 mm to about 9 mm, about 2 mm to about 8 mm, and/or about 3 mm to about 7 mm, for example. - The lyophilization device can include a plurality of
heat sinks 101 that individually have aheat sink surface 102 in thermal communication with a refrigerant 103. In such a lyophilization device, theheat sinks 101 can be disposed vertically in the lyophilization chamber with respect to each other, forming upper and lower heat sinks 101 (see e.g.,Figure 1 ). By convention, the lowerheat sink surface 102 is disposed between the upper and lower heat sinks and thetray surface 107 is disposed between theupper heat sink 101 and the lowerheat sink surface 102. In this arrangement, thethermal insulator 108 is disposed between thetray surface 107 and thelower heat sink 101. - In another embodiment, each
individual sample container 106 can sit on or be carried by a thermal insulator 108 (see e.g.,Figure 4b ). For example, when the sample container is a vial having a top and a bottom thethermal insulator 108 can comprise a thermally insulatingsupport 114 affixed to the bottom of the vial 115 (see e.g.,Figure 4c ). The thermally insulatingsupport 114 can have a thermal conductivity less than about 0.2 W/mK, less than about 0.1 W/mK, and/or less than about 0.05 W/mK at 25 °C, for example. In one embodiment, thevial 106 and the insulatingsupport 114 are different materials (e.g., the vial can comprise a glass and the insulating support can comprise a foam or a polymer). The vial can comprise a sealable vial. - The invention is directed to a method of freezing a liquid solution for subsequent lyophilization. In one embodiment of the method, the lyophilization chamber as described above is loaded with a liquid solution held in a container that includes an active pharmaceutical agent solute and a solvent. The liquid solution will have a
top surface 116 and a bottom surface, wherein thebottom surface 117 is proximal to the heat sink 101 (seeFigure 5 ). The container is separated from theheat sink 101 by providing athermal insulator 108 between the container and theheat sink 101, the thermal insulator having the characteristics described herein. Thus, the container is spaced vertically from the heat sink with an interveningthermal insulator 108, the distance andthermal insulator 108 being selected to provide freezing of the liquid solution from the top and bottom surfaces at approximately the same rate. Having been loaded into the lyophilization chamber, the liquid solution can be frozen by lowering the temperature of theheat sink 101 and thereby the ambient temperature in the lyophilization chamber. The liquid solution advantageously can be frozen from the top and the bottom surfaces at approximately the same rate to form a frozen solution. A further advantage is that the concurrent water to ice conversion at the top and bottom of the solution avoids problematic freeze-concentration and skin formation observed when the bottom of the solution freezes more rapidly than the top. - A further embodiment of the inventions includes once frozen, the liquid solution (now the frozen solution) can be lyophilized to yield a lyophilized cake. In one type of embodiment, the solution is lyophilized without any significant change in the
thermal insulator 108 such as by example maintaining the physical arrangement of the container and heat sink elements. In another type of embodiment, the container having the frozen liquid solution is placed in thermally-conductive contact with the heat sink during or following freezing, for example by removing thethermal insulator 108 and placing thetray 107 or containers directly on the shelf. Embodiments of the removal can comprise, removing thespacer 111, moving thebrackets 112 or altering the length of the struts (not shown). It is also envisioned that the thermal insulator container not be placed in thermally conductive contact with the heat sink but the insulation characteristics of thethermal insulator 108 be altered such as by significantly lessening the insulation characteristics by reducing the spacing between the tray and heat sink to a minimal distance. - As noted in connection with Example 2 below, when freezing and drying an array of containers, containers placed at the edges of such an array, and those especially at the corners, can experience temperatures which deviate from those of center containers, due to radiant heat from side walls. Thus, in a method of freezing an array of containers, it is contemplated that the
thermal insulator 108 or portions thereof between one or more of the container and heat sink can dimensionally vary from the thermal insulator or portions thereof between one or more remaining containers. In an embodiment, the thickness of thethermal insulator 108 can be reduced for edge and/or corner containers, relative to the thickness of thethermal insulator 108 between center containers and heat sink, in order to counter-balance the radiant heating experienced by such edge and corner containers from side walls and thus achieve more consistent temperature profiles across the array. - In this embodiment, the thermal insulator provides for the facile freezing of the liquid solution from the top and the bottom within the lyophilization chamber at approximately the same rate. The freezing of the liquid solution from the top and the bottom can be determined by measuring the temperature of the solution during the freezing process. The temperature can be measured by inserting at least two thermocouples into a vial containing the solution. A
first thermocouple 118 can be positioned at the bottom of the solution, at about the center of the vial, for example, and asecond thermocouple 119 can be positioned at the top of the solution, just below the surface of the solution, in about the center of the vial, for example. Once a freezing cycle has been optimized for a combination of liquid solution, container configuration, and lyophilization chamber, then in subsequent processing of additional batches temperature monitoring of the containers (e.g. vials) is not necessary. - To freeze the liquid solution from the top and the bottom surfaces at approximately the same rate, the thermal insulator (e.g., type and thickness) can be selected to provide a water-ice conversion index value in a range of about -2 °C to about 2 °C, or about -1 °C to about 1 °C, and/or about -0.5 °C to about 0.5 °C. Preferably, the water-ice conversion index is zero or a positive value. The water-ice conversion index is determined by a method including first plotting the temperatures reported by the thermocouples at the top (Tt) and at the bottom (Tb) of the solution as a function of time. The water-ice conversion index is the area between the curves, in °C•minute, between a first nucleation event and the end of water-ice conversion divided by the water-ice conversion time, in minutes. The water-ice conversion time is the time necessary for the temperature at the top (Tt) of the solution to reduce in value below the freezing point plateau for the solution.
- The temperature data are collected by loading solution-filled vials into a lyophilization chamber. The lyophilization tray, at t=0 min, is then cooled to about -60 °C. The temperature can then be recorded until a time after which the top and the bottom of the solution cool to a temperature below the freezing point plateau.
- The areas, positive and negative, are measured from the first nucleation event (observable in the plot of temperatures, e.g., such as in
Figure 6 ) 122 until both temperature values cool below thefreezing point plateau 123. The sum of these areas provides the area between the curves. When calculating the area between the curves, the value is positive when the temperature at the bottom of the vial (Tb) is warmer than the temperature at the top of the vial (Tt) 120 and the value is negative when the temperature at the top of the vial (Tt) is warmer than the temperature at the bottom of the vial (Tb) 121. Preferably, the water-ice conversion index is zero or a positive value. This condition will prevent the consequence that the freezing rate at the bottom of the solution is significantly higher than that at the top of the solution. Thus, for example, the water-ice conversion index value in one type of embodiment will be in a range of about 0°C to about 2°C, or about 0°C to about 1°C, or about 0°C to about 0.5°C. For a particular solution and container configuration, the cooling rate, temperature of the tray, and the thermal insulator can be optimized to provide an area between the curves at or near 0 °C•minute. For example,Figure 7 shows the water-ice conversion indices for 5 wt.% aqueous solutions of sucrose in vials on a stainless steel tray as a function of the distance from the heat sink surface to the stainless steel tray, with thethermal insulator 108 comprising air within a gap between the heat sink surface and the bottom of the stainless steel tray. The tray had a thickness of about 1.2 mm. - Still another embodiment of the invention is a lyophilized cake made by a method disclosed herein. The lyophilized cake can include a substantially dry lyophilized material and a plurality of pores in the lyophilized material having substantially the same pore size. In one embodiment, the lyophilized cake has a pore size that is substantially larger than the pore size of a reference lyophilized cake comprising the same material as the lyophilized cake but made by a standard lyophilization process (e.g., placing a
vial 106 comprising a liquid solution onto aheat sink 101 within a lyophilization chamber, excluding a thermal insulator between the vial and theheat sink 101, lowering the temperature of theheat sink 101 and thereby freezing the liquid solution, and then lyophilizing the frozen solution). The cross-sectional area of the cylindrical pores of the lyophilized cake is preferably at least 1.1, 2, and/or 3 times greater than the cross-sectional area of the reference lyophilized cake. In another embodiment the lyophilized cake has a substantially consistent pore size throughout the cake. - The size of pores in the lyophilized cake can be measured by a BET surface area analyzer. The effective pore radius (re), a measure of the pore size, can be calculated from the measured surface area of the pores (SSA) by assuming cylindrical pores. The effective pore radius re can be determined by the equation re = 2ε/SSA•ρs•(1-ε) where SSA is the surface area of the pores, ε is the void volume fraction or porosity (ε=Vvoid/Vtotal=n•re 2/Vtotal), (1-ε) is the solute concentration in the volume fraction units, and ρs is the density of the solid.
- The following examples are provided to illustrate the invention, but are not intended to limit the scope thereof.
- The effect of gap freezing on the pore enlargement for a lyophilized 10% aqueous sucrose solution was studied. Multiple 20 mL Schott tubing vials were filled with 7 mL of a 10% aqueous solution of sucrose. These filled vials were placed in a LyoStar II[tm] (FTS SYSTEMS, INC. Stone Ridge, NY) freeze dryer either directly in contact with a top shelf (heat sink surface) or on a 6mm gapped tray. See e.g.,
Fig. 1 . Multiple probed vials were produced by inserting two thermocouples into the solutions, one at the bottom-center of the vial and the other one about 2mm below the liquid surface. See.Fig. 5 . The filled vials were then lyophilized by the following procedure: - 1) the shelf was cooled to 5 °C and held at this temperature for 60 minutes; next
- 2) the shelf was cooled to -70 °C and held at this temperature for 200 minutes (the internal temperatures of the thermocouple-containing vials were recorded during freezing);
- 3) after freezing, the 6mm gapped tray was removed and these vials were placed directly on the bottom shelf (this provided the vials on the top and bottom shelves with the same shelf heat transfer rate during lyophilization, and thereby a direct comparison of the effect of different freezing methods could be performed); next
- 4) the lyophilization chamber was evacuated to a set-point of 9332.57 mPa (70 mTorr), and
- 5) a primary drying cycle, during which time the internal temperatures of the frozen samples were recorded, was started. The primary drying cycle involved (a) holding the samples for 10 minutes at -70 °C and 9332.57 (70 mTorr), then (b) raising the temperature at a rate of 1 °C/min to -40 °C while maintaining 9332.57 mPa (70 mTorr), then (c) holding the samples for 60 minutes at -40 °C and 9332.57 mPa (70 mTorr), then (d) raising the temperature at a rate of 0.5 °C/min to -25 °C while maintaining 9332.57 mPa (70 mTorr), and then (e) holding the samples for 64 hours at -25 °C and 6666.12 mPa (50 mTorr);
- 6) a secondary drying followed, and involved raising the temperature at a rate of 0.5 °C/min to 30 °C and 13332.2 mPa (100 mTorr), and then holding the samples for 5 hours at 30 °C and 13332.2 mPa (100 mTorr).
- The average product temperatures for the frozen samples in vials on the top and bottom (gapped-tray) shelves, during primary drying, are presented in
Figure 8 . It can be seen that the temperature profile of the samples on the bottom shelf is much lower than that of those on the top shelf, which implies that the pore size in the dry layer of the bottom shelf samples is much larger than those on the top shelf, due to the effect of "gap-freezing." Theoretically, the temperatures are different from the set point temperatures due to evaporative cooling and/or the insulative effect of larger pore sizes. - The effective pore radius, re, for the individual lyophilized cakes was determined by a pore diffusion model. See Kuu et al. "Product Mass Transfer Resistance Directly Determined During Freeze-Drying Using Tunable Diode Laser Absorption Spectroscopy (TDLAS) and Pore Diffusion Model." Pharm. Dev. Technol. (available online at: http://www.ncbi.nlm.nih.Qov/pubmed/20387998 and later published in Vol. 16, no. 4, p. 343-357, 2011). The results are presented in
Figure 9 , where it can be seen that the pore radius of the cakes on the bottom shelf is much larger than that on the top shelf. The results demonstrate that the 6mm gapped tray is very effective for pore enlargement. - An alternative lyophilization procedure was developed to increase the rate of freeze-drying by removing the gap between heat sink shelf and container-loaded shelf following freezing.
- Multiple 20 mL Schott tubing vials were filled with 5 mL of a 5% (w/v) aqueous solution of sucrose. Two trays containing these filled vials were placed in a LyoStar II™ (FTS SYSTEMS, INC. Stone Ridge, NY) freeze dryer in the upper and lower portions of the chamber. The trays were separated from contact with the heat sink shelves by a thermal insulator comprising a spacer made of plastic tubing placed on each heat sink shelf, to provide a gap of approximately 6.5mm between each tray and each heat sink shelf.
- For monitoring the product temperature on each shelf, two thermocouples were placed in center vials and six thermocouples were placed on the edge locations of the shelves, as shown in
Figures 10 and 11 , wherein the numbers indicate temperature-probed vials. - The shelf temperature (each) was cooled to -70° C, followed by holding the shelf at -70°C for 90 minutes. At this low shelf temperature, cooling of vials can be accelerated, since cooling with a gap is primarily driven by radiation. The shelf was then heated to -50° C, followed by holding the shelf at -50°C for 60 minutes. After the solution was frozen the shelf temperature was raised to a higher temperature of -50°C because after complete freezing of the solution it is not necessary to maintain it at - 70oC for vacuum pulling. For one of the trays, the
thermal insulator 108 was removed prior to vacuum pulling by removing the spacer. - For primary drying: (a) the lyophilization chamber was then evacuated to a set-point of 13332.2 mPa (100 mTorr), (b) the shelf temperature was held at -50°C (at 13332.2 mPa (100 mTorr)) for 30 minutes; (c) the shelf temperature was then ramped to -15°C (at 13332.2 mPa (100 mTorr)) at a rate of 0.5 °C/min; and (d) the shelf temperature was then held at -15°C (at 13332.2 mPa (100 mTorr)) until the end of primary drying.
- For secondary drying: (e) the shelf temperature was ramped to 30 °C (at 13332.2 mPa (100 mTorr)), at a rate of 0.5 °C/min; and (f) the shelf temperature was then held at 30 °C (at 13332.2 mPa (100 mTorr)) until the end of secondary drying.
- Only the temperature profiles of the center vials (TP01, TP02, TP09 and TP10) and the edge vials along the side walls (TP04, TP07, TP12, and TP15) are used for comparison. The product temperature profiles of the corner vials (TP03, TP05, TP06, TP08, TP11, TP13, TP14, and TP16) are not representative for a manufacturing scale freeze dryer due to the strong thermal radiation from the front and back walls to corner vials in this freeze dryer. The front wall of the LyoStar™ II freeze dryer is acrylic without insulation. The back wall of the chamber has insulation, but the large amount of heat produced by the fluid pump penetrates through the insulation and raises the product temperature to some extent.
- As shown in
Figs. 12 and13 , the drying time on the top shelf (Fig. 12 , thermal insulator remaining during vacuum pulling) is much longer than that on the bottom shelf (Fig. 13 , thermal insulator removed before vacuum pulling) due to the much higher heat transfer rate on the bottom shelf without a thermal insulator. It can be seen fromFig. 12 that after approximate 2670 minutes of cycle time, primary drying was still not complete, since the temperature in the center vial, TP02 did not move out of the plateau level during primary drying. On the other hand,Fig. 13 shows that after approximate 1690 minutes of cycle time, primary drying was complete, since the temperatures in the center vials, TP09 and TP10 moved out of the plateau levels of primary drying. Inlet temperatures of the shelf refrigerant fluids are plotted as Tf on each ofFigures 12 and13 . - The comparison is shown in
Fig. 14 , in which the difference between TP02 and TP09 is about 1.7°C. - The comparison is shown in
Fig. 15 , in which the difference between TP02 and TP07 is about 1.5°C. - The comparison is shown in
Fig. 16 , in which the difference between TP09 and TP12 is only about 0.2°C, which is much smaller than 1.5°C on the top shelf. - Using the same lyophilization cycle, the vials on the tray without a thermal insulator between the tray and shelf during drying are dried much faster than those with a thermal insulator between the tray and shelf during drying. The tray without a thermal insulator during drying also has the advantage of reducing the temperature difference between the center and edge vials, which could be important for some temperature-sensitive formulations.
- The foregoing description is given for clearness of understanding only, and no unnecessary limitations should be understood therefrom, as modifications within the scope of the invention may be apparent to those having ordinary skill in the art.
Claims (15)
- A method comprising:providing a lyophilization chamber comprising a heat sink surface in thermal communication with a refrigerant (103);loading a container (106) comprising a liquid solution into the lyophilization chamber above the heat sink surface, the liquid solution comprising an active pharmaceutical agent solute and a solvent, the liquid solution having a top surface (116) and a bottom surface (117);forming a thermal conduction insulator (108) between the bottom of the container and the heat sink surface to isolate the container from thermal conductivity with the heat sink;lowering the temperature of the heat sink and thereby the ambient temperature in the lyophilization chamber comprising the container to a temperature sufficient to freeze the liquid solution,the thermal conduction insulator selected to provide freezing of the liquid solution from the top and the bottom surfaces at approximately the same temperature and thereby form a frozen solution; and reducing the ambient pressure in the chamber to lyophilize the frozen solution after altering the thermal conduction insulator;
characterised in that the method comprises: during or after freezing, altering the thermal conduction insulator. - The method of claim 1, wherein the thermal conduction insulator (108) comprises one of air, a gas, or vacuum space.
- The method of claim 1, wherein the thermal conduction insulator has a thermal conductivity less than about 0.2 W/mK.
- The method of claim 2, further comprising providing a tray (110) upon which the container rests between the container and thermal conduction insulator, the tray optionally being thermally conductive or thermally insulating.
- The method of claim 1, wherein the heat sink comprises a refrigerant conduit in thermal communication with the heat sink surface.
- The method of claim 1, wherein the container comprises a vial optionally, wherein the thermal conduction insulator (108) comprises a thermally insulating support member affixed to the bottom of the vial, and the thermally insulating support member rests on the heat sink.
- The method of claim 1, wherein the lyophilization chamber includes at least two parallel heat sinks (101) and further comprising loading the container (106) comprising the liquid solution into the lyophilization chamber between the two parallel heat sinks at distances spaced vertically from each heat sink with an intervening thermal conduction insulator (108), the distances and thermal conduction insulator selected to provide freezing the liquid solution from the top (116) and the bottom (117) surfaces at approximately the same temperature and thereby form a frozen solution.
- The method of claim 1, further comprising placing the container (106) on a tray (110) wherein the thermal conduction insulator (108) comprises a separation distance between the tray and heat sink (101) optionally, wherein the altering step comprises thermally contacting the tray (110) and heat sink (101).
- The method of claim 1, wherein the altering step comprises placing the container (106) comprising frozen liquid solution in thermally-conductive contact with the heat sink (101).
- The method of claim 1 wherein the forming step includes placing at least one spacer (111) between the container (106) and heat sink (101) and the altering step includes removing the at least one spacer.
- The method of claim 10, further comprising placing the container (106) on a tray (110) wherein the thermal conduction insulator (108) comprises a separation distance between the tray and heat sink (101) and the at least one spacer (111) is disposed between the tray and heat sink.
- The method of claim 8 wherein the contacting step comprises contacting after freezing.
- The method of claim 1, wherein the thermal conduction insulator (108) is altered after freezing the liquid solution in the container (106).
- The method of claim 1, wherein the thermal conduction insulator (108) is altered during freezing the liquid solution in the container (106).
- The method of claim 1, wherein the thermal conduction insulator (108) is altered to lessen the insulation characteristics.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP16200274.5A EP3171109B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP16200274.5A EP3171109B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
| PCT/US2012/030854 WO2013147759A1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
| EP12716817.7A EP2831526B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
Related Parent Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12716817.7A Division-Into EP2831526B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
| EP12716817.7A Division EP2831526B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3171109A1 EP3171109A1 (en) | 2017-05-24 |
| EP3171109B1 true EP3171109B1 (en) | 2018-11-14 |
Family
ID=46001741
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12716817.7A Not-in-force EP2831526B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
| EP16200274.5A Not-in-force EP3171109B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12716817.7A Not-in-force EP2831526B1 (en) | 2012-03-28 | 2012-03-28 | Optimization of nucleation and crystallization for lyophilization using gap freezing |
Country Status (5)
| Country | Link |
|---|---|
| EP (2) | EP2831526B1 (en) |
| DE (1) | DE112012006137T8 (en) |
| ES (1) | ES2626001T3 (en) |
| GB (1) | GB2516191A (en) |
| WO (1) | WO2013147759A1 (en) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US8689460B2 (en) * | 2010-09-28 | 2014-04-08 | Baxter International Inc. | Optimization of nucleation and crystallization for lyophilization using gap freezing |
| EP3218661B1 (en) | 2014-11-14 | 2020-02-12 | Project Pharmaceutics GmbH | Freeze drying of nested vials |
| EP3250868B1 (en) * | 2015-01-28 | 2020-07-15 | IMA Life North America Inc. | Process monitoring and control using battery-free multipoint wireless product condition sensing |
| BR112017016138A2 (en) | 2015-01-28 | 2018-07-10 | Ima Life North America Inc | process control using noninvasive printed product sensors |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4501719A (en) * | 1981-05-04 | 1985-02-26 | Marquest Medical Products, Inc. | Tray apparatus for freeze-drying biologicals having a predetermined unit dosage |
| FR2623277B1 (en) * | 1987-11-17 | 1990-04-27 | Bioetica Sa | LYOPHILIZATION METHOD AND APPARATUS COMPRISING THERMAL SHIELDING MEANS BETWEEN LYOPHILIZATION SHELVES |
| US8371039B2 (en) * | 2009-12-30 | 2013-02-12 | Baxter International Inc. | Thermal shielding to optimize lyophilization process for pre-filled syringes or vials |
| US8689460B2 (en) * | 2010-09-28 | 2014-04-08 | Baxter International Inc. | Optimization of nucleation and crystallization for lyophilization using gap freezing |
-
2012
- 2012-03-28 DE DE112012006137.3T patent/DE112012006137T8/en not_active Expired - Fee Related
- 2012-03-28 GB GB1419097.9A patent/GB2516191A/en not_active Withdrawn
- 2012-03-28 ES ES12716817.7T patent/ES2626001T3/en active Active
- 2012-03-28 EP EP12716817.7A patent/EP2831526B1/en not_active Not-in-force
- 2012-03-28 EP EP16200274.5A patent/EP3171109B1/en not_active Not-in-force
- 2012-03-28 WO PCT/US2012/030854 patent/WO2013147759A1/en not_active Ceased
Non-Patent Citations (1)
| Title |
|---|
| None * |
Also Published As
| Publication number | Publication date |
|---|---|
| EP2831526A1 (en) | 2015-02-04 |
| DE112012006137T5 (en) | 2015-01-15 |
| GB201419097D0 (en) | 2014-12-10 |
| GB2516191A (en) | 2015-01-14 |
| EP2831526B1 (en) | 2017-02-22 |
| DE112012006137T8 (en) | 2015-02-19 |
| WO2013147759A1 (en) | 2013-10-03 |
| EP3171109A1 (en) | 2017-05-24 |
| ES2626001T3 (en) | 2017-07-21 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US9528761B2 (en) | Optimization of nucleation and crystallization for lyophilization using gap freezing | |
| EP2622293B1 (en) | Optimization of nucleation and crystallization for lyophilization using gap freezing | |
| Konstantinidis et al. | Controlled nucleation in freeze‐drying: Effects on pore size in the dried product layer, mass transfer resistance, and primary drying rate | |
| EP2831526B1 (en) | Optimization of nucleation and crystallization for lyophilization using gap freezing | |
| KR20190035808A (en) | Methods and apparatus for freezing-drying and containers | |
| US10101085B2 (en) | Directional freezing | |
| Jadhav et al. | Review on lyophilization technique | |
| Kuu et al. | Gap-freezing approach for shortening the lyophilization cycle time of pharmaceutical formulations—demonstration of the concept | |
| JP2545592B2 (en) | Method and apparatus for freeze-drying viscous solution | |
| Southard et al. | Heat transfer characteristics of sublimation from frozen thin films | |
| CN104949473B (en) | A kind of vacuum freeze drier and vacuum freeze-drying method | |
| GB2400901A (en) | Method and apparatus for freeze drying material | |
| Rosa et al. | Improving heat transfer at the bottom of vials for consistent freeze drying with unidirectional structured ice | |
| CN111479465A (en) | Apparatus and method involving freezing at least a portion of a biological sample | |
| Stapley | Freeze drying | |
| Nakagawa | Mathematical Modeling of Freeze‐Drying Process | |
| Shaozhi et al. | A thermophysical study on the freeze drying of wooden archaeological artifacts | |
| Matejčíková et al. | Impact of packing density on primary drying rate | |
| Khairnar et al. | International Journal of Research in Pharmacy and Science | |
| Oddone et al. | Control of freezing as a mean for process intensification in freeze-drying |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AC | Divisional application: reference to earlier application |
Ref document number: 2831526 Country of ref document: EP Kind code of ref document: P |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20171124 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: F26B 5/06 20060101AFI20180302BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20180525 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AC | Divisional application: reference to earlier application |
Ref document number: 2831526 Country of ref document: EP Kind code of ref document: P |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 1065325 Country of ref document: AT Kind code of ref document: T Effective date: 20181115 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602012053674 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20181114 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1065325 Country of ref document: AT Kind code of ref document: T Effective date: 20181114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190214 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190314 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190214 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190215 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190314 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602012053674 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20190815 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190328 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20190331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190328 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190331 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190331 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20120328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181114 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20240220 Year of fee payment: 13 Ref country code: GB Payment date: 20240220 Year of fee payment: 13 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602012053674 Country of ref document: DE |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20250328 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20251001 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250328 |