EP2732089B1 - Verfahren zum herstellen einer beschickungstür sowie beschickungstür für eine wäschebehandlungsmaschine - Google Patents
Verfahren zum herstellen einer beschickungstür sowie beschickungstür für eine wäschebehandlungsmaschine Download PDFInfo
- Publication number
- EP2732089B1 EP2732089B1 EP12729164.9A EP12729164A EP2732089B1 EP 2732089 B1 EP2732089 B1 EP 2732089B1 EP 12729164 A EP12729164 A EP 12729164A EP 2732089 B1 EP2732089 B1 EP 2732089B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- door
- frame
- support regions
- loading door
- viewing pane
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Classifications
-
- D—TEXTILES; PAPER
- D06—TREATMENT OF TEXTILES OR THE LIKE; LAUNDERING; FLEXIBLE MATERIALS NOT OTHERWISE PROVIDED FOR
- D06F—LAUNDERING, DRYING, IRONING, PRESSING OR FOLDING TEXTILE ARTICLES
- D06F39/00—Details of washing machines not specific to a single type of machines covered by groups D06F9/00 - D06F27/00
- D06F39/12—Casings; Tubs
- D06F39/14—Doors or covers; Securing means therefor
Definitions
- the invention is in the field of equipment and machines which are used for treating, in particular for drying and / or washing, laundry or other objects and which are generally referred to below as laundry treatment machines.
- the invention relates to a method for producing a loading door for a laundry treatment machine with a door frame and a sight glass held in the door frame, on which a seal is applied, wherein the door frame is formed at least by joining at least one frame inner part with at least one frame outer part, and the sight glass between the frame inner part and the frame outer part is introduced such that it is supported with at least one support surface on a plurality of door frame side support areas.
- the invention further relates to a loading door for a laundry treatment machine having a door frame comprising at least one frame inner part and a frame outer part, and with a sight glass arranged in the door frame, which rests at least partially on contact areas of the door frame and on which a seal is applied.
- a door frame which comprises at least one frame inner part and at least one outer frame part joined thereto. Between the frame parts, an insert is held and introduced in such a way that it is supported with at least one support surface on a plurality of door frame side support areas.
- Insert is a preferably cup-shaped glass (sight glass), the edge of which is received in a circumferential gap or receiving space formed by the frame parts.
- the receiving space is dimensioned so that enough clearance is available to compensate for production-related deviations in the actual measure of the thickness of the glass safely.
- a seal is arranged between the frame inner part and the glass pane, which ensures a secure seal by its elasticity and its cross-section and also compensates for said manufacturing tolerances of the insert by a more or less strong axial compression.
- the actual thickness of the door frame may vary by design if the elasticity of the seal is insufficient to completely compensate for any dimensional deviations of the insert thickness.
- an object of the present invention is to specify a method for producing a loading door or in the creation of a loading door, is provided by or in which a tolerance compensation of the insert dimensions such that the thickness of the loading door always in a predetermined Target dimension is adjustable and thus design specifications can be met to the effect that, for example, the frame inner part and the frame outer part at predetermined edges without joints and gap lie on each other.
- the material of the bearing areas is brought into a temporarily plastically deformable state before joining the frame parts, forces are applied to the bearing areas with inserted sight glass, so that they are so deformed by deformation of the geometry of the sight glass adjust that a given target amount of door thickness is adjusted, wherein the door thickness, the frame parts, which comprises between these inserted sight glass and the seal, and wherein the bearing areas then brought back into an undeformable (solid) state and the frame parts are joined.
- a first significant advantage of the invention is thus that as well comparatively large tolerances can be accepted, in particular, in the dimensions of the insert that are relevant for the loading door thickness, because these are compensated for individually by displacement, erosion or deformation of the material of the door frame-side support areas. This also has a positive effect on the production costs because higher tolerances in the actual thickness of the insert are acceptable as a result.
- the inventive method is also characterized by a simple feasibility and automation, because advantageously at the same time applied to the forces exerted on the door frame parts on these forces can also serve for deformation or shape adaptation / Vertikalwashanpassung the support areas.
- the bearing areas After the bearing areas have again been brought into a substantially non-deformable or solid state-for example, a hardened or solidified state-they can reliably exert their supporting and holding functions in a geometry optimally adapted to the shape of the bearing surface of the insert.
- a method of manufacturing a loading door which meets even the most demanding specifications regarding the gauge size of the loading door and the design specifications - e.g. a gapless joining of the door frame parts in the externally visible area (for example on the door frame lateral surface) - is sufficient.
- the insert is brought into a prestressed position which is withdrawn with respect to the support areas during the joining and is released again after completion of the joining.
- a bias is applied to the usually provided between inserts such as sight glasses and a frame part seal and thus creates a tight fit between the insert and the respective support area.
- the insert sight glass
- the insert can be detected by a suction cup and drawn in the direction of biasing.
- the inventive temporary plastic deformability of at least the bearing areas can basically be realized by various physical and / or chemical methods.
- a dissolving or softening of the support areas by a solvent or by (thermal) energy supply is conceivable.
- the bearing areas or particularly preferably the frame inner part and the frame outer part are made of a thermoplastic material.
- these can preferably be provided with cooperating connecting webs, which are heated together with the support areas and plastically deformed or connected.
- a so-called heating mirror between the joining partners (frame inner part and frame outer part) can be positioned, so that the thermoplastic material melts due to the heat energy thus supplied. Then, the heating mirror is removed and the frame parts are placed on each other (joined) such that the cooperating connecting webs merge with each other.
- the respective support region is adapted to the geometry of the insert or the support surface such that excess material is displaced.
- the loading door manufacturing technology can be particularly elegant and expedient brought to a predetermined target thickness.
- the support areas consist of a temporarily plastically deformable material and that the support areas are plastically deformed by the joining of the frame parts such that adjusts a predetermined target amount of door thickness, compensating for component tolerances of the sight glass, wherein the door thickness comprises the frame parts, the sight glass inserted between them and the seal.
- frame inner part and frame outer part preferably made of a thermoplastic material and have cooperating connecting webs.
- the insert may be a glass sheet or a so-called sight glass, e.g. can be made in a conventional manner from a preferably transparent plastic or silicate.
- the advantages of the invention are also realized and / or preferred in the case of an (additional further) insert which comprises an element extending to the inside of the door, such as a signal transmitter or a locking element.
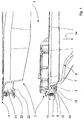
- FIG. 1 shows a fragmentary sectional view of essential elements of a loading door 1 according to the invention prior to their final assembly or joining.
- the loading door 1 comprises a door frame 2, which consists of at least one frame inner part 3 and a (in FIG. 1 not yet joined) frame outer part 4 is formed. Between the frame parts 3, 4, an insert 6 is arranged in the form of a sight glass 7 already inserted into the frame inner part 3, which is held after the joining between the frame parts.
- the sight glass 7 has a circumferential edge 8, which comprises a door frame inside bearing surface 9 and a door frame outer side bearing surface 10.
- the sight glass 7 rests on a previously applied to a circumferential ridge 12 or rolled-up seal 14, which provides with an inside sealing lip 15 in a conventional manner for a sealing closure of a feed opening, not shown, a laundry treatment machine through the loading door 1.
- the support surface 10 is supported in the mounted state of the loading door several doorframe side support areas 20 from, of which in FIG. 1 by way of example only, a support portion of a substantially radially extending rib or ridge 21 is shown.
- At least the support regions 20 are made of a material 22 which is temporarily plastically deformable.
- Both the frame inner part 3 and the frame outer part 4 are made of a thermoplastic material.
- At least the supporting regions 20 are brought into a temporarily plastically deformable state, for example by introducing heat.
- a so-called (in FIG. 1 not shown) heating mirror are introduced, which specifically heats the areas of the frame parts 3, 4 to be softened due to its adapted geometry.
- the sight glass 7 is gripped at its curvature by a suction cup, not shown, and pulled in the direction of arrow 24 vertically downwards. Due to the elastic deformation of the seal 14, the insert 6 (sight glass 7) is thus in a prestressed position, which has a somewhat decreasing effect on the material removal or on the material displacement in the region of the support regions 20.
- the frame parts are preferably made by thermoplastic fusion of connecting webs (as described below in connection with FIGS FIG. 3 even more detailed) and as in FIG. 2 shown connected. How out FIG. 2 can be seen in the region of the support region 20, this is optimally adapted to the geometry of the sight glass 7, ie, on the geometry and the shape of the support surface 10 by the targeted melting described above. After re-hardening of the thermoplastic material, the rib 21 forms a strong and highly resilient support for the sight glass 7. After removal of the bias by removing the suction cup, the door seal 14 resiliently against the direction of the arrow 24 elastically rebound again, resulting in a tight interference fit between support surface 10 and the corresponding cooperating contact surface 25 of the support area 20 leads.
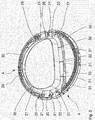
- FIG. 3 shows in further detail the joining principle and the adjustment of the nominal dimension of the door thickness in a perspective view
- the insert 6 (FIG. FIG. 1
- One recognizes several distributed over the circumference holding or support webs 21, of which representative a support web 21 in connection with the FIGS. 1 and 2 has been described in detail.
- the remaining support webs are at their support areas 20 in a corresponding manner to the individual geometry and tolerant thickness of (in FIG. 3 Not shown) use adapted by melting.
- It also recognizes a substantially circumferential, corrugated connecting web 30 and a further connecting web 31, which cooperate with correspondingly formed and complementarily positioned connecting webs of the frame inner part 3 when joining the frame parts.
- FIG. 4 shows in an approximately radial view increases the area A from FIG. 3 , It can be seen a centering post 40 and on both sides arranged posts 41, 42 with an approximately cross-shaped cross section and formed at their respective free end support areas 43, 44. On these support areas 43, 44 is a support surface of a functional insert, such as a signal transmitter pin, using a Frame interior fixed and stored.
- a functional insert such as a signal transmitter pin
- FIG. 5 shows in sectional view with attached insert 50, penetrates the centering post 40 a corresponding receiving bore 52 of a door frame inner part 54, which may be formed integrally with the insert 50 as shown in this embodiment.
- On the inside bearing surfaces 55, 56 of the insert 50 are based on the support areas 43, 44, which made in a corresponding manner by previously done heating the material of the posts 41, 42 temporarily plastically deformable have been prepared and so to a tolerance compensating removal or displacement of the material.
- the insert and thus a functional element 57 is brought into the desired desired position.
Landscapes
- Engineering & Computer Science (AREA)
- Textile Engineering (AREA)
- Wing Frames And Configurations (AREA)
- Securing Of Glass Panes Or The Like (AREA)
- Automobile Manufacture Line, Endless Track Vehicle, Trailer (AREA)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102011078918A DE102011078918A1 (de) | 2011-07-11 | 2011-07-11 | Verfahren zum Herstellen einer Beschickungstür sowie Beschickungstür für eine Wäschebehandlungsmaschine |
| PCT/EP2012/062306 WO2013007510A1 (de) | 2011-07-11 | 2012-06-26 | Verfahren zum herstellen einer beschickungstür sowie beschickungstür für eine wäschebehandlungsmaschine |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2732089A1 EP2732089A1 (de) | 2014-05-21 |
| EP2732089B1 true EP2732089B1 (de) | 2016-09-21 |
Family
ID=46331356
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP12729164.9A Active EP2732089B1 (de) | 2011-07-11 | 2012-06-26 | Verfahren zum herstellen einer beschickungstür sowie beschickungstür für eine wäschebehandlungsmaschine |
Country Status (5)
| Country | Link |
|---|---|
| EP (1) | EP2732089B1 (pl) |
| CN (1) | CN103649404B (pl) |
| DE (1) | DE102011078918A1 (pl) |
| PL (1) | PL2732089T3 (pl) |
| WO (1) | WO2013007510A1 (pl) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102024104001A1 (de) * | 2024-02-13 | 2025-08-14 | Miele & Cie. Kg | Tür für eine Wäschebehandlungsmaschine, Wäschebehandlungsmaschine und Verfahren zur Herstellung einer Wäschebehandlungsmaschine |
Family Cites Families (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10031172A1 (de) * | 2000-06-27 | 2002-01-10 | Bsh Bosch Siemens Hausgeraete | Dichtungseinrichtung |
| DE10031171A1 (de) * | 2000-06-27 | 2002-01-10 | Bsh Bosch Siemens Hausgeraete | Bullaugen-Fenster für eine Frontlader-Trommelwaschmaschine |
| DE10053413A1 (de) * | 2000-10-27 | 2002-05-08 | Bsh Bosch Siemens Hausgeraete | Bullaugentür für eine von vorn beschickbare Trommelwaschmaschine |
| US20050262681A1 (en) * | 2004-06-01 | 2005-12-01 | Lg Electronics Inc. | Door of drum washer and assembling method for the same |
| KR101125402B1 (ko) * | 2004-07-19 | 2012-03-27 | 엘지전자 주식회사 | 드럼 세탁기의 도어 구조 |
| DE102005023445A1 (de) | 2005-05-20 | 2006-11-23 | BSH Bosch und Siemens Hausgeräte GmbH | Tür für eine Wäschetrockenmaschine |
| ITTO20050453A1 (it) * | 2005-06-29 | 2006-12-30 | Indesit Co Spa | Sportello per elettrodomestico in particolare per macchina, lavasciuga o asciugabiancheria a carica frontale o sostanzialmente frontale |
| JP4551299B2 (ja) * | 2005-09-08 | 2010-09-22 | パナソニック株式会社 | ドラム式洗濯機 |
| CN101497242A (zh) * | 2008-01-28 | 2009-08-05 | 株式会社比体昂恩得丕 | 滚筒洗衣机门制造方法 |
| CN201245778Y (zh) * | 2008-08-13 | 2009-05-27 | 松下电化住宅设备机器(杭州)有限公司 | 滚筒洗衣机机门 |
| JP4845058B2 (ja) * | 2008-08-28 | 2011-12-28 | シャープ株式会社 | ドラム式洗濯機 |
| CN201411566Y (zh) * | 2009-05-13 | 2010-02-24 | 松下家电研究开发(杭州)有限公司 | 机门结构及采用该机门结构的滚筒洗衣机 |
| EP2253756B1 (en) * | 2009-05-22 | 2014-05-14 | Electrolux Home Products Corporation N.V. | Manufacturing method of a door unit, in particular a door unit for a laundry treating machine |
| JP5618517B2 (ja) * | 2009-09-30 | 2014-11-05 | 日立アプライアンス株式会社 | 電気洗濯機 |
| EP2405051B1 (en) * | 2010-07-06 | 2014-07-02 | Electrolux Home Products Corporation N.V. | Glass porthole window for laundry washing and/or drying appliance |
-
2011
- 2011-07-11 DE DE102011078918A patent/DE102011078918A1/de not_active Withdrawn
-
2012
- 2012-06-26 PL PL12729164T patent/PL2732089T3/pl unknown
- 2012-06-26 WO PCT/EP2012/062306 patent/WO2013007510A1/de not_active Ceased
- 2012-06-26 CN CN201280034268.6A patent/CN103649404B/zh active Active
- 2012-06-26 EP EP12729164.9A patent/EP2732089B1/de active Active
Also Published As
| Publication number | Publication date |
|---|---|
| DE102011078918A1 (de) | 2013-01-17 |
| CN103649404B (zh) | 2016-03-30 |
| EP2732089A1 (de) | 2014-05-21 |
| RU2014101773A (ru) | 2015-11-27 |
| PL2732089T3 (pl) | 2017-02-28 |
| CN103649404A (zh) | 2014-03-19 |
| WO2013007510A1 (de) | 2013-01-17 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102014114086B4 (de) | System zur elastisch gemittelten Ausrichtung | |
| EP2486288B1 (de) | Verbindung zwischen zwei bauteilen aus verstärktem kunststoff und verfahren zu ihrer herstellung | |
| DE102008010197B4 (de) | Verfahren zum Verbinden von zwei Rumpfsektionen unter Schaffung eines Querstoßes sowie Querstoßverbindung | |
| DE102012019849B4 (de) | Bauteil mit Dichtstopfen sowie Verfahren zum Einformen eines Bauteileinsatzes | |
| DE102009044210A1 (de) | Dübel und Verfahren zur Montage eines Dübels in eine Leichtbauplatte | |
| DE102008021788A1 (de) | Verfahren zum Reparieren einer Flugzeugkomponente | |
| WO2013135414A1 (de) | Bauteilverbindung | |
| EP2860407B1 (de) | Strukturbauteil | |
| EP3100848B1 (de) | Faserkunststoffverbund-bauteil mit verdichteten fasern und verfahren zu dessen herstellung | |
| DE102014112003A1 (de) | Montageeinheit und Verfahren zu deren Herstellung | |
| DE19753111A1 (de) | Lagerbuchse mit Mittelbund sowie deren Verwendung und Herstellungsverfahren | |
| EP3134254A1 (de) | Verfahren zum verbinden von verbindungsabschnitten von wenigstens zwei bauteilen | |
| EP3339632A1 (de) | Anschluss- und befestigungseinheit für einen blitzrezeptor zur integration in ein windenergieanlagenrotorblatt | |
| DE102016124078B3 (de) | Verbindungsanordnung für die Verbindung von zwei Schaltschrankrahmengestellen | |
| WO2013007510A1 (de) | Verfahren zum herstellen einer beschickungstür sowie beschickungstür für eine wäschebehandlungsmaschine | |
| EP1394420A2 (de) | Einsatzteil für eine Wandöffnung, insbesondere an einer Fahrzeugkarosserie | |
| DE102016225911B4 (de) | Nockenwellenmodul sowie Verfahren zum Herstellen eines Nockenwellenmoduls | |
| DE102017222950A1 (de) | Gehäuse für einen Gassack eines Fahrzeuginsassen-Rückhaltesystems eines Kraftfahrzeugs, formgebende Vorrichtung und Verfahren zum Herstellen eines derartigen Gehäuses | |
| EP2639395B1 (de) | Rahmenprofil, Flügel eines Fensters oder einer Tür und Verfahren zur Herstellung desselben | |
| DE102012015606A1 (de) | Abstandselement und Verfahren zur relativen Ausrichtung | |
| EP2642059A1 (de) | Verfahren zum Verstärken eines Kunststoff-Hohlkammerprofils | |
| DE102005043997B4 (de) | Bauteilsatz zum Bilden eines zusammengesetzten Bauteils und Einsatzbauteil | |
| DE102024001349A1 (de) | Verbindung zwischen einer Außenhaut-Beplankung und eines Fahrzeug-Rohbaus | |
| WO2017067538A1 (de) | Schweissbaugruppe und verfahren zur herstellung einer schweissbaugruppe | |
| DE102016002958A1 (de) | Vorrichtung zum Befestigen einer Leitung, Dichteinsatz |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20140211 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: BSH HAUSGERAETE GMBH |
|
| 17Q | First examination report despatched |
Effective date: 20150814 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20160513 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 831152 Country of ref document: AT Kind code of ref document: T Effective date: 20161015 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502012008311 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D Ref country code: NL Ref legal event code: MP Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161221 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161222 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170123 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20161221 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20170121 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502012008311 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| 26N | No opposition filed |
Effective date: 20170622 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20180228 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170630 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170630 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170626 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170630 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20170630 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 831152 Country of ref document: AT Kind code of ref document: T Effective date: 20170626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20120626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20160921 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R084 Ref document number: 502012008311 Country of ref document: DE |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20230622 Year of fee payment: 12 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20240626 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240626 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250630 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20250618 Year of fee payment: 14 |