EP2475796B1 - Piece metallique pourvue de renforts fibreux a extremite biseautee et son procédé de fabrication - Google Patents
Piece metallique pourvue de renforts fibreux a extremite biseautee et son procédé de fabrication Download PDFInfo
- Publication number
- EP2475796B1 EP2475796B1 EP10810744.2A EP10810744A EP2475796B1 EP 2475796 B1 EP2475796 B1 EP 2475796B1 EP 10810744 A EP10810744 A EP 10810744A EP 2475796 B1 EP2475796 B1 EP 2475796B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- metal
- rectilinear
- fibrous reinforcement
- fibrous reinforcements
- mechanical part
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C47/00—Making alloys containing metallic or non-metallic fibres or filaments
- C22C47/02—Pretreatment of the fibres or filaments
- C22C47/04—Pretreatment of the fibres or filaments by coating, e.g. with a protective or activated covering
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C47/00—Making alloys containing metallic or non-metallic fibres or filaments
- C22C47/02—Pretreatment of the fibres or filaments
- C22C47/025—Aligning or orienting the fibres
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C47/00—Making alloys containing metallic or non-metallic fibres or filaments
- C22C47/02—Pretreatment of the fibres or filaments
- C22C47/06—Pretreatment of the fibres or filaments by forming the fibres or filaments into a preformed structure, e.g. using a temporary binder to form a mat-like element
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C47/00—Making alloys containing metallic or non-metallic fibres or filaments
- C22C47/20—Making alloys containing metallic or non-metallic fibres or filaments by subjecting to pressure and heat an assembly comprising at least one metal layer or sheet and one layer of fibres or filaments
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22F—WORKING METALLIC POWDER; MANUFACTURE OF ARTICLES FROM METALLIC POWDER; MAKING METALLIC POWDER; APPARATUS OR DEVICES SPECIALLY ADAPTED FOR METALLIC POWDER
- B22F2998/00—Supplementary information concerning processes or compositions relating to powder metallurgy
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y10—TECHNICAL SUBJECTS COVERED BY FORMER USPC
- Y10T—TECHNICAL SUBJECTS COVERED BY FORMER US CLASSIFICATION
- Y10T428/00—Stock material or miscellaneous articles
- Y10T428/13—Hollow or container type article [e.g., tube, vase, etc.]
- Y10T428/131—Glass, ceramic, or sintered, fused, fired, or calcined metal oxide or metal carbide containing [e.g., porcelain, brick, cement, etc.]
- Y10T428/1314—Contains fabric, fiber particle, or filament made of glass, ceramic, or sintered, fused, fired, or calcined metal oxide, or metal carbide or other inorganic compound [e.g., fiber glass, mineral fiber, sand, etc.]
Definitions
- the invention relates to a metal part provided with fibrous reinforcements.
- WO 2009/034264 a connecting rod manufactured as follows: producing a metal blank comprising two elongate slots parallel on either side of a plane of symmetry of the connecting rod; inserting into the housing fibrous reinforcements made from carbide fibers sheathed with a metal compatible with that of the container; evacuation and hot isostatic compression of the assembly allowing an intimate connection of the fibers of the fibrous reinforcement with the metal of the blank by metal diffusion around the fibers.
- the metal sheathing the carbide fibers melts and mixes with the metal near the metal preform to achieve a metal continuum intimately encompassing the fibers of the fibrous reinforcements. It then remains to machine the blank to get the connecting rod (including the drilling holes screeds).
- the documents FR2946550 and DE102004001262 describe annular mechanical parts comprising a metal matrix reinforced with ceramic fibers.
- the fibrous reinforcements have at least one end completely embedded in the metal of the part and which has an end face transverse to the fibers. At this level, there is in the piece a steep jump of rigidity, and the transmission of mechanical stresses between the fibrous reinforcements and the container may give rise to detachments or tearing likely to form the start of cracks.
- the internal stresses are, in this area, generally perpendicular to the fibers, so that this zone is weakened.
- the invention aims to provide metal mechanical parts provided with at least one fibrous reinforcement, wherein the aforementioned drawback is reduced or eliminated.
- the mechanical part is manufactured from a metal blank having at least one housing extending substantially in one direction preferred stress force experienced by the mechanical part in use, and wherein at least one fibrous reinforcement is inserted and intimately bonded to the blank by a metal diffusion around the fibers of the fibrous reinforcement so as to have at least one end completely embedded in the metal of the room.
- the said end is beveled according to two slopes.
- the interface extending at the end of the fibrous reinforcement between the latter and the metal of the blank is oblique relative to the forces passing through the mechanical part, which allows a gradual adaptation of the rigidity of the part following the direction of the fibrous reinforcements. This arrangement mitigates the risk of separation of the fibrous reinforcement with the rest of the metal.
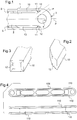
- the rod of the invention is, according to a first embodiment, made from a metal blank 1 here of generally flat shape and having a running portion 2 of constant section terminated by two end portions 3 rounded forming End caps and having through holes 4.
- the blank is made of titanium alloy.
- Longitudinal housings 5 extend here parallel to a plane of symmetry P of the blank 1, on either side of it, and form housings adapted to receive fibrous reinforcements 10 (the fibrous reinforcements have been represented cut to better show housing, but in reality, they occupy the dwellings over their entire length).
- the plane of symmetry P is parallel to a preferred direction of introduction of forces into the connecting rod (essentially traction and compression forces in the axis of the connecting rod).
- the fibrous reinforcements comprise longitudinally extending fibers.
- the fibers are titanium-sheathed silicon carbide fibers.
- the fibers are secured to each other before being placed in the grooves by subjecting them to hot isostatic compression.
- the housings 5 have ends 11 oblique with respect to the plane of symmetry P, and here extend parallel to a plane P 'tangential to the adjacent through hole.
- the oblique ends 11 can be obtained in various ways.
- the grooves are machined in the metal blank over its entire length, so that the grooves open on the edge of the blank.
- there is a titanium plug having a beveled end portion defining the beveled end of the corresponding housing, the plugs being preferably placed after the positioning of the fibrous reinforcements in the grooves.
- the plugs may consist of a piece of titanium in one block, or be made by compacting a metal powder.
- the fibrous reinforcements have a shape complementary to that of the housings, and comprise an end 12 bevelled in two slopes compatible with the oblique end of the housing.
- the fibrous reinforcements 10 are covered by titanium alloy blocks filling the housing 5. These blocks may be provided integral plugs closing the housing.
- the sealed assembly is evacuated, before being subjected to hot isostatic pressing, so that the metal cladding of the fibers melts and diffuses to form a metal compound with the metal of the blank and blocks, thus ensuring an intimate connection between the fibers and the surrounding metal.
- a metal matrix composite part is thus formed.
- the bevel of the end of the fibrous reinforcements which is completely embedded in the metal of the part allows a transmission of forces between the end of the fibers and the surrounding metal which is no longer only in tearing, but in shear, which reduces the risk of separation of the fibers at this level, and create a transition zone avoiding a leap of too much stiffness. Achieving a beveled end in two slopes avoids the formation of a thin tip that weakens the fiber reinforcement during handling.
- the figure 4 illustrates a rod 101 which is provided with four fibrous reinforcements 110.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Materials Engineering (AREA)
- Mechanical Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Crystallography & Structural Chemistry (AREA)
- Manufacture Of Alloys Or Alloy Compounds (AREA)
- Pressure Welding/Diffusion-Bonding (AREA)
- Shafts, Cranks, Connecting Bars, And Related Bearings (AREA)
- Insertion Pins And Rivets (AREA)
Description
- L'invention est relative à une pièce métallique pourvue de renforts fibreux.
- On connaît du document
WO 2009/034264 une bielle fabriquée de la façon suivante : réalisation d'une ébauche métallique comportant deux logements oblongs parallèles de part et d'autre d'un plan de symétrie de la bielle ; insertion dans les logements de renforts fibreux réalisés à partir de fibres de carbure gainées d'un métal compatible avec celui du conteneur ; mise sous vide et compression isostatique à chaud de l'ensemble permettant une liaison intime des fibres du renfort fibreux avec le métal de l'ébauche par diffusion métallique autour des fibres. - Le métal gainant les fibres de carbure fond et se mélange au métal voisin de la préforme métallique pour réaliser un continuum métallique englobant de façon intime les fibres des renforts fibreux. Il reste alors à usiner l'ébauche pour obtenir la bielle (notamment le perçage des orifices des chapes). Les documents
FR2946550 DE102004001262 décrivent des pièces mécaniques annulaire comprenant une matrice métallique renforcée par des fibres céramiques. En général, les renforts fibreux présentent au moins une extrémité complètement noyée dans le métal de la pièce et qui présente une face terminale transversale aux fibres. A ce niveau, il existe dans la pièce un saut de rigidité abrupt, et la transmission des contraintes mécaniques entre les renforts fibreux et le conteneur risque de donner lieu à des décollements ou des arrachements susceptibles de former le départ de criques. Qui plus est, les contraintes internes sont, dans cette zone, généralement perpendiculaires aux fibres, de sorte que cette zone est affaiblie. - L'invention vise à proposer des pièces mécaniques en métal pourvues d'au moins un renfort fibreux, dans lequel l'inconvénient précité est atténué, voire éliminé.
- A cet effet, on propose une pièce mécanique selon la revendication 2 et un procédé de fabrication de ladite pièce selon la revendication 1. La pièce mécanique est fabriquée à partir d'une ébauche métallique présentant au moins un logement s'étendant sensiblement selon une direction privilégiée d'effort subie par la pièce mécanique en service, et dans laquelle au moins un renfort fibreux est inséré puis intimement lié à l'ébauche par une diffusion métallique autour des fibres du renfort fibreux de sorte à présenter au moins une extrémité complètement noyée dans le métal de la pièce. Selon l'invention, la dite extrémité est biseautée selon deux pentes.
- Ainsi, l'interface s'étendant à l'extrémité du renfort fibreux entre ce dernier et le métal de l'ébauche est oblique relativement aux efforts transitant dans la pièce mécanique, ce qui permet une adaptation progressive de la rigidité de la pièce en suivant la direction des renforts fibreux. Cette disposition atténue les risques de désolidarisation du renfort fibreux avec le reste du métal.
-
- la
figure 1 est une vue schématique de dessus d'une bielle; - la
figure 2 est une vue en perspective de l'extrémité d'un des renforts fibreux, selon l'invention; - la
figure 3 est une vue en perspective de dessus de l'extrémité d'un renfort fibreux - la
figure 4 est une vue de face et de dessus d'une bielle. - Dans l'explication qui suit, la réalisation des renforts fibreux n'est pas l'objet de l'invention et ne sera donc pas décrite en détail. On pourra se référer par exemple au document
WO2009/034264 qui décrit plusieurs modes de réalisation de tels renforts fibreux. - En référence à la
figure 1 , la bielle de l'invention est, conformément à un premier mode de réalisation, réalisée à partir d'une ébauche métallique 1 ici de forme généralement plate et présentant une partie courante 2 de section constante terminée par deux parties d'extrémité 3 arrondies formant des chapes d'extrémité et comportant des orifices traversants 4. Ici, l'ébauche est en alliage de titane. - Des logements longitudinaux 5 s'étendent ici parallèlement à un plan de symétrie P de l'ébauche 1, de part et d'autre de celui-ci, et forment des logements adaptés à recevoir des renforts fibreux 10 (les renforts fibreux ont été représentés coupés pour mieux faire apparaître les logements, mais en réalité, ils occupent les logements sur toute leur longueur). On remarquera que le plan de symétrie P est parallèle à une direction privilégiée d'introduction d'efforts dans la bielle (essentiellement des efforts de traction et de compression dans l'axe de la bielle).
- Les renforts fibreux 10 comprennent des fibres s'étendant longitudinalement. Ici, les fibres sont des fibres de carbure de silicium gainées de titane. De préférence, les fibres sont solidarisées entre elles avant mise en place dans les rainures en leur faisant subir une compression isostatique à chaud.
- Selon l'invention, les logements 5 ont des extrémités 11 obliques par rapport au plan de symétrie P, et s'étendent ici parallèlement à un plan P' tangent à l'orifice traversant adjacent. Les extrémités obliques 11 peuvent être obtenues de diverses manières. De façon préférée, les rainures sont usinées dans l'ébauche métallique sur toute sa longueur, de sorte que les rainures débouchent sur le chant de l'ébauche. Puis on rapporte à chaque extrémité de rainure un bouchon en titane, ayant une partie terminale biseautée définissant l'extrémité biseautée du logement correspondant, les bouchons étant de préférence mis en place après le positionnement des renforts fibreux dans les rainures. Les bouchons peuvent être constitués d'un morceau de titane en un seul bloc, ou être réalisés par compactage d'une poudre métallique.
- Selon l'invention, les renforts fibreux ont une forme complémentaire de celle des logements, et comportent une extrémité 12 en biseau selon deux pentes compatible avec l'extrémité oblique du logement.
- Les renforts fibreux 10 sont recouverts par des blocs en alliage de titane venant combler les logements 5. Ces blocs peuvent être prévus solidaires des bouchons fermant les logements.
- Puis l'ensemble rendu étanche est mis sous vide, avant d'être soumis à une compression isostatique à chaud, de sorte que le gainage métallique des fibres fonde et diffuse pour former un composé métallique avec le métal de l'ébauche et des blocs, assurant ainsi une liaison intime entre les fibres et le métal environnant. On forme ainsi une pièce composite à matrice métallique.
- Le biseau de l'extrémité des renforts fibreux, qui est complètement noyé dans le métal de la pièce permet une transmission d'efforts entre l'extrémité des fibres et le métal environnant qui ne soit plus uniquement en arrachement, mais en cisaillement, ce qui permet de diminuer le risque de désolidarisation des fibres à ce niveau, et de créer une zone de transition évitant un saut de raideur trop important. La réalisation d'une extrémité biseautée selon deux pentes permet d'éviter la formation d'une pointe fine qui fragilise le renfort fibreux lors de sa manipulation.
- La
figure 4 illustre une bielle 101 qui est pourvue de quatre renforts fibreux 110. - On notera bien évidement que le biseau de l'invention n'a pas strictement rien à voir avec le biseau mentionné dans le document
EP1726678 , qui désigne l'angle de coupe de l'extrémité de la nappe de renfort, et qui sert à imprimer un angle d'hélice à la nappe lors de sa pose. On notera qu'en tout état de cause, cette extrémité est tangente au bord de la pièce tubulaire recouverte par la nappe et qu'elle n'est donc pas noyée.
Claims (2)
- Procédé de fabrication d'une pièce mécanique à partir d'une ébauche métallique (1) comprenant les étapes suivantes :a) réaliser au moins un logement (5) rectiligne dans l'ébauche métallique (1), le logement (5) s'étendant selon une direction privilégiée d'effort subie par la pièce mécanique en service ;b) insérer au moins un renfort fibreux (10) rectiligne dans le logement (5) ;c) lier le renfort fibreux (10) à l'ébauche métallique (1) par diffusion métallique autour des fibres du renfort fibreux (10) rectiligne de sorte qu'au moins une des extrémités du renfort fibreux (10) rectiligne soit entièrement noyée dans le métal formant la pièce mécanique ;la au moins une extrémité (12) du renfort fibreux (10) rectiligne noyée dans le métal formant la pièce mécanique étant biseautée selon deux pentes.
- Pièce mécanique comprenant un renfort fibreux (10) rectiligne lié à une ébauche métallique (1) par diffusion métallique autour des fibres du renfort fibreux (10) rectiligne de sorte qu'au moins une des extrémités du renfort fibreux (10) rectiligne soit entièrement noyée dans le métal formant la pièce mécanique, l'extrémité du renfort fibreux (10) rectiligne noyée dans le métal formant la pièce mécanique étant biseautée selon deux pentes.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR0904370A FR2950078B1 (fr) | 2009-09-11 | 2009-09-11 | Piece metallique pourvue de renforts fibreux a extremite biseautee. |
| PCT/EP2010/005593 WO2011029619A2 (fr) | 2009-09-11 | 2010-09-13 | Piece metallique pourvue de renforts fibreux a extremite biseautee |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2475796A2 EP2475796A2 (fr) | 2012-07-18 |
| EP2475796B1 true EP2475796B1 (fr) | 2018-09-05 |
Family
ID=42077141
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP10810744.2A Active EP2475796B1 (fr) | 2009-09-11 | 2010-09-13 | Piece metallique pourvue de renforts fibreux a extremite biseautee et son procédé de fabrication |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US20120251744A1 (fr) |
| EP (1) | EP2475796B1 (fr) |
| CN (1) | CN102597293B (fr) |
| BR (1) | BR112012005444A2 (fr) |
| CA (1) | CA2773032C (fr) |
| FR (1) | FR2950078B1 (fr) |
| RU (1) | RU2509172C2 (fr) |
| WO (1) | WO2011029619A2 (fr) |
Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6009843A (en) * | 1997-10-22 | 2000-01-04 | 3M Innovative Properties Company | Fiber reinforced, titanium composite engine valve |
| DE102004001262A1 (de) * | 2004-01-08 | 2005-08-04 | Mtu Aero Engines Gmbh | Verfahren und Vorrichtung zum Ablegen von Fasern in Ausnehmungen, insbesondere bei der Herstellung von MMC-Bauteilen |
| FR2946550A1 (fr) * | 2009-06-16 | 2010-12-17 | Messier Dowty Sa | Procede de fabrication d'une piece metallique incorporant un renfort annulaire fibreux. |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3902864A (en) * | 1970-06-03 | 1975-09-02 | Gen Dynamics Corp | Composite material for making cutting and abrading tools |
| EP0558869A1 (fr) * | 1992-03-02 | 1993-09-08 | Gebrüder Sulzer Aktiengesellschaft | Objet comportant une surface abrasive et procédé pour sa fabrication |
| US6568061B2 (en) * | 2001-09-21 | 2003-05-27 | Atlantic Research Corporation | Method for controlling composite preform elements during processing |
| FR2886290B1 (fr) * | 2005-05-27 | 2007-07-13 | Snecma Moteurs Sa | Procede de fabrication d'une piece avec un insert en materiau composite a matrice metallique et fibres ceramiques |
| FR2886181B1 (fr) * | 2005-05-27 | 2008-12-26 | Snecma Moteurs Sa | Procede de fabrication d'une piece tubulaire avec un insert en materiau composite a matrice metallique |
| FR2886180B1 (fr) * | 2005-05-27 | 2007-07-13 | Snecma Moteurs Sa | Procede de fabrication d'une nappe liee constituee de fils ceramiques a matrice metallique, dispositif de mise en oeuvre du procede nappe liee obtenue par le procede |
| FR2919284B1 (fr) * | 2007-07-26 | 2010-09-24 | Snecma | Piece mecanique comportant un insert en materiau composite. |
| FR2919283B1 (fr) * | 2007-07-26 | 2010-09-17 | Snecma | Piece mecanique comportant un insert en materiau composite. |
| FR2925896B1 (fr) * | 2007-12-28 | 2010-02-05 | Messier Dowty Sa | Procede de fabrication d'une piece metallique renforcee de fibres ceramiques |
-
2009
- 2009-09-11 FR FR0904370A patent/FR2950078B1/fr active Active
-
2010
- 2010-09-13 EP EP10810744.2A patent/EP2475796B1/fr active Active
- 2010-09-13 CN CN201080040591.5A patent/CN102597293B/zh active Active
- 2010-09-13 RU RU2012114001/02A patent/RU2509172C2/ru not_active IP Right Cessation
- 2010-09-13 WO PCT/EP2010/005593 patent/WO2011029619A2/fr not_active Ceased
- 2010-09-13 CA CA2773032A patent/CA2773032C/fr active Active
- 2010-09-13 BR BR112012005444A patent/BR112012005444A2/pt not_active IP Right Cessation
- 2010-09-13 US US13/395,357 patent/US20120251744A1/en not_active Abandoned
Patent Citations (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US6009843A (en) * | 1997-10-22 | 2000-01-04 | 3M Innovative Properties Company | Fiber reinforced, titanium composite engine valve |
| DE102004001262A1 (de) * | 2004-01-08 | 2005-08-04 | Mtu Aero Engines Gmbh | Verfahren und Vorrichtung zum Ablegen von Fasern in Ausnehmungen, insbesondere bei der Herstellung von MMC-Bauteilen |
| FR2946550A1 (fr) * | 2009-06-16 | 2010-12-17 | Messier Dowty Sa | Procede de fabrication d'une piece metallique incorporant un renfort annulaire fibreux. |
Also Published As
| Publication number | Publication date |
|---|---|
| US20120251744A1 (en) | 2012-10-04 |
| FR2950078B1 (fr) | 2012-10-05 |
| CN102597293A (zh) | 2012-07-18 |
| FR2950078A1 (fr) | 2011-03-18 |
| BR112012005444A2 (pt) | 2016-04-12 |
| CA2773032A1 (fr) | 2011-03-17 |
| RU2012114001A (ru) | 2013-10-20 |
| CA2773032C (fr) | 2015-04-21 |
| CN102597293B (zh) | 2014-03-19 |
| WO2011029619A2 (fr) | 2011-03-17 |
| EP2475796A2 (fr) | 2012-07-18 |
| WO2011029619A3 (fr) | 2011-05-05 |
| RU2509172C2 (ru) | 2014-03-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0216405B1 (fr) | Rivet notamment pour matériaux composites | |
| EP0398403B1 (fr) | Organe de rivetage aveugle, procédé d'assemblage et assemblages obtenus | |
| CA2710547C (fr) | Procede de fabrication d'une piece metallique renforcee de fibres ceramiques | |
| EP2445705A2 (fr) | Procédé de fabrication de bielles composites et bielles obtenues selon le procédé | |
| CA2729377C (fr) | Procede de fabrication d'une piece metallique renforcee de fibres ceramiques | |
| WO2008142311A1 (fr) | Procédé de fabrication d'un rivet et rivet obtenu selon ce procédé | |
| EP1537993B1 (fr) | Procédé de réalisation d'une structure stratifiée et avion muni d'une telle structure | |
| JP2015083870A (ja) | 構造構成部品 | |
| CA2932963A1 (fr) | Lame d'entrainement de crochets appartenant a une mecanique jacquard et mecanique jacquard comprenant une telle lame | |
| FR2553690A1 (fr) | Methode d'assemblage d'un tube mince dans une plaque ou un manchon | |
| FR2754556A1 (fr) | Procede de renforcement d'un ouvrage de construction, et ouvrage ainsi renforce | |
| CA2773032C (fr) | Piece metallique pourvue de renforts fibreux a extremite biseautee | |
| EP2370702B1 (fr) | Procede de fabrication d'une bielle en metal, renforcee par des fibres longues | |
| FR2863185A1 (fr) | Dispositif d'equipement d'un trou dans un panneau et panneau ainsi equipe | |
| FR3049490A1 (fr) | Procede et dispositif d'implantation d'un insert dans une plaque composite | |
| EP2475899B1 (fr) | Procede de fabrication d'une bielle metallique renfocee par des fibres, et bielle ainsi obtenue | |
| FR2864829A1 (fr) | Composite a matrice de ceramique a resistance laminaire amelioree, et procede pour celui-ci | |
| WO2014013166A1 (fr) | Procede de brasage de pieces en materiau composite avec integration d'un pion dans la liaison | |
| FR3037859A1 (fr) | Dispositif et procede de production d'un element multicouche | |
| CN103057065A (zh) | 注塑机的拉杆机构 | |
| FR3147607A1 (fr) | Assemblage comportant au moins une pièce composite et des moyens de fixation | |
| FR2891283A1 (fr) | Tige d'axe et lame | |
| EP0206856A1 (fr) | Joint nipplé biconique fileté pour électrodes de four à arc électrique | |
| FR2596833A1 (fr) | Disque de friction renforce | |
| FR3065382A1 (fr) | Outil d'usinage et procede d'usinage associe |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20120308 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| DAX | Request for extension of the european patent (deleted) | ||
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: DUNLEAVY, PATRICK Inventor name: FRANCHET, JEAN-MICHEL Inventor name: MASSON, RICHARD Inventor name: KLEIN, GILLES |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SAFRAN LANDING SYSTEMS |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: SAFRAN LANDING SYSTEMS |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20170504 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20180328 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 1037890 Country of ref document: AT Kind code of ref document: T Effective date: 20180915 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: FRENCH |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602010053408 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20180905 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181205 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181206 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20181205 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1037890 Country of ref document: AT Kind code of ref document: T Effective date: 20180905 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190105 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20190105 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602010053408 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20180930 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180913 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180913 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| 26N | No opposition filed |
Effective date: 20190606 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180930 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180930 Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20100913 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20180905 Ref country code: MK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20180905 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250919 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20250923 Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250923 Year of fee payment: 16 |