EP2137476B1 - Apparatus for drying tiles - Google Patents
Apparatus for drying tiles Download PDFInfo
- Publication number
- EP2137476B1 EP2137476B1 EP08737368A EP08737368A EP2137476B1 EP 2137476 B1 EP2137476 B1 EP 2137476B1 EP 08737368 A EP08737368 A EP 08737368A EP 08737368 A EP08737368 A EP 08737368A EP 2137476 B1 EP2137476 B1 EP 2137476B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- drying
- tiles
- blowing
- suction
- unit
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
Images

Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F26—DRYING
- F26B—DRYING SOLID MATERIALS OR OBJECTS BY REMOVING LIQUID THEREFROM
- F26B5/00—Drying solid materials or objects by processes not involving the application of heat
- F26B5/12—Drying solid materials or objects by processes not involving the application of heat by suction
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F26—DRYING
- F26B—DRYING SOLID MATERIALS OR OBJECTS BY REMOVING LIQUID THEREFROM
- F26B15/00—Machines or apparatus for drying objects with progressive movement; Machines or apparatus with progressive movement for drying batches of material in compact form
- F26B15/10—Machines or apparatus for drying objects with progressive movement; Machines or apparatus with progressive movement for drying batches of material in compact form with movement in a path composed of one or more straight lines, e.g. compound, the movement being in alternate horizontal and vertical directions
- F26B15/12—Machines or apparatus for drying objects with progressive movement; Machines or apparatus with progressive movement for drying batches of material in compact form with movement in a path composed of one or more straight lines, e.g. compound, the movement being in alternate horizontal and vertical directions the lines being all horizontal or slightly inclined
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F26—DRYING
- F26B—DRYING SOLID MATERIALS OR OBJECTS BY REMOVING LIQUID THEREFROM
- F26B5/00—Drying solid materials or objects by processes not involving the application of heat
- F26B5/14—Drying solid materials or objects by processes not involving the application of heat by applying pressure, e.g. wringing; by brushing; by wiping
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F26—DRYING
- F26B—DRYING SOLID MATERIALS OR OBJECTS BY REMOVING LIQUID THEREFROM
- F26B2210/00—Drying processes and machines for solid objects characterised by the specific requirements of the drying goods
- F26B2210/02—Ceramic articles or ceramic semi-finished articles
Definitions
- the invention relates to an apparatus for drying tiles exiting a wet processing line, such as, for example, a smoothing, a chamfering, a squaring, or other linens.
- Apparatuses for drying tiles are known comprising roller conveyors on which the tiles to be dried are conveyed through a drying zone in which air suction ports are provided that face one another in a direction that is perpendicular to the surface of the lower face and to the surface of the upper face of the tile and which are able to suck from such surfaces drops of water that may be present' thereupon.
- blades made of rubber positioned so as to rub on the surfaces to be dried and thus to remove a certain quantity of water therefrom.
- a drawback of such apparatus is that the blades made of rubber become worn very rapidly and thus need to be replaced frequently.
- a further drawback is that the blades are not effective on tiles that have irregular surfaces, because in such tiles there may be surface, irregularities that the blades are unable to penetrate.
- the air suction ports are supported at a fixed distance from the conveying plane defined by the rollers and are therefore at a distance from the surfaces to be dried that depends on the thickness of the tiles.
- the ports may consequently be positioned, for tiles of a certain thickness, at a functionally correct distance from the surfaces to be dried, whilst, for tiles of lesser thickness, this distance may be insufficient to ensure appropriate drying.
- FR 1 121 791 A discloses a drying apparatus having a combination of elements as set forth in the of the appended preamble claim 1.
- An object of the invention is to improve apparatuses for drying tiles.
- a further object of the invention is to make more effective apparatuses that are able to dry tiles that have irregular surfaces.
- a still further object of the invention is to make apparatuses that enable tiles that have different thicknesses to be dried in succession.
- the apparatus 1 comprises first moving means 3 arranged for moving the tiles 2 towards a drying zone 4.
- the first moving means 3 comprises a first belt 5 that supports and moves, the tiles 2 to the drying zone 4 along an advance direction A1.
- the first moving means 3 may comprise a roller conveyor provided with a plurality of driven rollers that enable the tiles 2 to be supported and moved to the drying zone 4.
- the apparatus 1 further comprises second moving means 43 arranged for moving the tiles 2 away from the drying zone 4.
- the second moving means 43 comprises a second belt 45 that supports and moves the tiles 2 away from the drying zone 4 along the advance direction A1.
- the second moving means 43 may comprise a roller conveyor provided with a plurality of driven rollers that enable the tiles 2 to be supported and moved to the drying zone 4.
- the third moving means 6 receives the tile 2 from the first moving means 3.
- the third moving means 6 comprises a plurality of rollers 8 rotatably supported by a frame 9 through supporting bars, which are not shown. In this way the rollers 8 enable the tiles 2 to be supported and moved through the drying zone 4.
- the frame 9 further comprises a first opening 10 placed at the entrance of the drying zone 4 and a second opening 40 placed at the outlet of the drying zone 4, further downstream than the first opening 10 according to the advance direction A1.
- the third moving means 6 is arranged near the first moving means 3 and the second moving means 43.
- the third moving means 6 is interposed between the first moving means 3 and the second moving means 43 according to the advance direction A1.
- the rollers 8 of the third moving means 6 define, together with the first belt 5 and the second belt 45, an advance plane P for the tiles 2.
- the tile 2 is easily transferred from the first moving means 3 to the third moving means 6, and enters the drying zone 4 through the first opening 10.
- the tile 2 is transferred from the third moving means 6 to the second moving means 43 and exits the drying zone 4 through the second opening 40.
- the third moving means 6 further comprises a strap 11 wound on a pair of pulleys 12.
- the pair of pulleys 12 supports the strap 11 and the rotation of the pair of pulleys 12 transmits motion to the strap 11.
- the strap 11 comprises an active part 13, which slides along a direction A2.
- the active part 13 of the strap 11 interacts with a peripheral portion 14 of the rollers 8.
- rollers 8 are rotated according to a rotation direction R1 and support a lower face 16 of the tiles 2 at a loading zone 15.
- the tiles 2 are thus supported and moved along the advance direction A1 owing to the rollers 8.
- the apparatus 1 further comprises drying means 17, positioned in the drying zone 4.
- the drying means 17 comprises a suction unit 18, that faces an upper face 19 of the tiles 2.
- the drying means 17 further comprises a blowing unit 20, that faces the upper face 19 of the tiles 2 in a position further downstream of the suction unit 18 along the advance direction A1.
- the suction unit 18 extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of the tile 2 in this direction. In this way the suction unit 18 is able to ensure suction along the entire width of the tile 2.
- the suction unit 18 has a section converging on the advance plane P, that has a distal region 21 with a greater section, an intermediate region 22 with a variable section and a proximal region 23 with a lesser section.
- the proximal region 23 directly faces the upper face 19 of the tile 2 and finishes with a lower end 25.
- the blowing unit 20 is structurally shaped like the suction unit 18.
- the blowing unit 20 thus extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of the tile 2 in this direction. In this manner the blowing unit 20 is able to ensure blowing along the entire width of the tile 2.
- the drying means 17 moves together with a positioning means 24.
- the positioning means 24 enables a constant distance D to be maintained between the upper face 19 of the tiles 2 and the lower end 25 of the drying means 17.
- the positioning means 24 comprises roller means 26 that is rotatably supported by the drying means 17 by supporting brackets 27.
- the supporting brackets 27 extend along the advance direction A1 and have a first end 28 fixed near the proximal region 23 and a second end 29 intended for rotatably supporting the roller means 26.
- the roller means 26 is thus at both sides of the proximal region 23, along the advance direction A1.
- the roller means 26 defines an interaction zone 30 at which the roller means 26 interacts with the upper face 19 of the tile 2 in transit and is induced to roll thereupon.
- the suction unit 18 is fixed to a supporting arm 31 by elastic connecting means that enables the suction means 18 to remain substantially in the same position with respect to the advance plane P when the supporting arm 31 performs rotations around an end 32 thereof, which is hinged on the frame 9 by further elastic connecting means.
- the elastic connecting means and the further elastic connecting means thus act as a hinge.
- the supporting arm 31 rotates around an axis Cl, that is perpendicular to the advance direction A1.
- the blowing unit 20 is fixed to a further supporting arm 33 through hinge means, that is not shown.
- the further supporting arm 33 is structurally and functionally shaped like the supporting arm 31.
- the suction unit 18 is connected to a first suction conduit 37 and the blowing unit 20 is connected to a first blowing conduit 38.
- the apparatus 1 further comprises further drying means 67, positioned in the drying zone 4 on the opposite side to the drying means 17 with respect to the tiles 2.
- the further drying means 67 comprises a further suction unit 68 that faces the lower face 16 of the tiles 2.
- the further suction unit 68 is arranged at the suction unit 18 in the space between consecutive rollers 8.
- the further suction unit 68 is structurally and functionally shaped like the suction unit 18.
- the further suction unit 68 then extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of the tile 2 in that direction. In this way the further suction unit 68 is able to ensure suction along the entire width of the tile 2.
- the suction unit 68 has a section converging on the advance plane P, and comprises a further distal region 71 with a greater section, a further intermediate region 72 with a variable section and further proximal region 73 with a lesser section.
- the further upper region 73 faces the lower face 16 of the tile 2 directly.
- the drying means 67 further comprises a further blowing unit 70, that faces the lower face 16 of the tiles 2 in a position further downstream of the further suction unit 68 along the advance direction A1.
- the further blowing unit 70 is arranged at the blowing unit 20 at a lesser vertical height.
- the further blowing unit 70 is structurally shaped like the blowing unit 20.
- the further blowing unit 70 thus extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of the tile 2 in that direction. In this way the blowing unit 70 is able to ensure blowing along the entire width of the tile 2.
- the further drying means 67 is fixed to the frame 9 through fixing means that is not shown.
- the further drying means 67 is arranged inside the drying zone 4 so that the further upper region 73, which directly faces the lower face 16, is positioned in the gap left between two successive rollers 8.
- the further suction unit 68 is connected to a second suction conduit 87 and the further blowing unit 70 is connected to a second blowing conduit 88.
- the first suction conduit 37 and the second suction conduit 87 are connected to a main suction conduit, which is not shown, which is in turn connected to the inlet of the filter means 89.
- the filter means 89 receives from the main suction conduit the air, in which there is a small quantity of water that was removed from the upper face 19 and from the lower face 16 of the tiles 2. The filter means 89 thus separates the air from the water present, which is collected in a collecting vessel, which is not shown.
- the filter means 89 is connected to fan means 90 through an inlet conduit, which is not shown.
- the fan means comprised the inlet conduit that is connected to the filter means 89 and a main blowing conduit, which is not shown.
- the fan means 90 further comprises a fan wheel, which is not shown, which is interposed between the inlet conduit and the main connecting conduit.
- the main blowing conduit is connected to the first blowing conduit 38 and to the second blowing conduit 88.
- the fan means 90 creates the pressure that is necessary for receiving from the filter means 89 the air purified of any trace of water.
- the fan means 90 further blows air to the blowing unit 20 and the further blowing unit 70. Initially, the air runs through the main blowing conduit and subsequently runs through the first blowing conduit 38 and the second blowing conduit 88.
- the fan means 90 provides high-pressure air. This causes the air to heat, which promotes completion of the drying of the tiles 2 by the blowing unit 20 and by the further blowing unit 70.
- the fan means 90 thus ensures both suction of the air through the suction unit 18 and the further suction unit 68 and blowing through the blowing unit 20 and the further blowing unit 70.
- Figure 3 shows an operating configuration X1 of the apparatus 1 in which the tile 2, which is in the drying zone 4, has an irregular surface on the upper face 19.
- the upper face 19 shows flat portions 96 arranged at different vertical heights that alternate randomly and are joined together by oblique portions 97.
- the positioning means 24 is in constant contact with the upper face 19 through the roller means 26.
- Figure 3 shows the suction unit 18 and the blowing unit 20, that are moved independently of one another, along a further direction A3 whilst the roller means 26 rolls on the upper face 19 following the profile thereof.
- the suction unit 18 and the blowing unit 20 face the flat portions 96, that are arranged at different vertical heights. In this way the suction unit 18 and the blowing unit 20 ensure complete drying of the upper face 19 of the tile 2.
- the drying means 17 and the further drying means 67 comprise blades made of rubber, mounted instead of the suction means 18 and/or of the blowing means 20. These blades differ from prior-art blades to be mounted on the supporting arms 31, 33 and cooperating with the roller means 26. In this way also these blades are maintained at a constant distance from the surface of the upper face 19.
- the wet tile 2 is supported and moved by the first moving means 3 to the drying zone 4, along the advance direction A1.
- the tile 2 reaches the first opening 10 of the frame 9 is transferred from the first moving means 3 to the third moving means 6, thus entering the drying zone 4.
- the rollers 8 of the third moving means 6 thus support the tile 2 and make the tile 2 proceed along the advance direction A1. Drying starts when the most advanced edge of the tile 2 meets the first roller of the roller means 26 lifting the first roller and thus taking the suction unit 18 to the envisaged height so as to maintain the distance D between the upper face 19 and the lower end 25 of the suction unit 18 constant, whatever the flat portion 96 that the suction unit 18 faces.
- the positioning means 24 of the blowing unit 20 forces the blowing unit 20 to be positioned at a precise vertical height.
- This vertical height is such as to maintain constant the distance D between the upper face 19 and the lower end 25 of the blowing unit 20, whatever the flat portion 96 that the blowing unit 20 faces.
- the positioning means 24 of the suction unit 18 continues to maintain the suction unit 18 at a vertical height such as to maintain the distance D constant. This also occurs if the vertical height of the flat portion 96 that the suction unit 18 faces, and the vertical height of the flat portion 96 that the blowing unit 20 faces, are different from one another.
- the apparatus 1 is able to dry successively the tiles 2 that have different thicknesses. Also in this configuration the distance D between the upper face 19 and the lower end 25 is maintained constant as the positioning means 24 is maintained in contact with the upper face 19 whatever the value of the thickness of the tile 2.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- General Engineering & Computer Science (AREA)
- Health & Medical Sciences (AREA)
- Life Sciences & Earth Sciences (AREA)
- Molecular Biology (AREA)
- Drying Of Solid Materials (AREA)
- Devices For Post-Treatments, Processing, Supply, Discharge, And Other Processes (AREA)
Abstract
Description
- The invention relates to an apparatus for drying tiles exiting a wet processing line, such as, for example, a smoothing, a chamfering, a squaring, or other linens. Apparatuses for drying tiles are known comprising roller conveyors on which the tiles to be dried are conveyed through a drying zone in which air suction ports are provided that face one another in a direction that is perpendicular to the surface of the lower face and to the surface of the upper face of the tile and which are able to suck from such surfaces drops of water that may be present' thereupon. In the drying zone there are further provided blades made of rubber positioned so as to rub on the surfaces to be dried and thus to remove a certain quantity of water therefrom.
- A drawback of such apparatus is that the blades made of rubber become worn very rapidly and thus need to be replaced frequently.
- A further drawback is that the blades are not effective on tiles that have irregular surfaces, because in such tiles there may be surface, irregularities that the blades are unable to penetrate.
- Further, when the blades slide on irregular surfaces they tend to become worn more rapidly.
- The air suction ports are supported at a fixed distance from the conveying plane defined by the rollers and are therefore at a distance from the surfaces to be dried that depends on the thickness of the tiles. The ports may consequently be positioned, for tiles of a certain thickness, at a functionally correct distance from the surfaces to be dried, whilst, for tiles of lesser thickness, this distance may be insufficient to ensure appropriate drying.
-
FR 1 121 791 Apreamble claim 1. - An object of the invention is to improve apparatuses for drying tiles.
- A further object of the invention is to make more effective apparatuses that are able to dry tiles that have irregular surfaces.
- A still further object of the invention is to make apparatuses that enable tiles that have different thicknesses to be dried in succession.
- According to the invention, there is provided an apparatus for drying tiles as defined in
claim 1. - The invention can be better understood and implemented with reference to the attached drawings, which illustrate an embodiment thereof by way of non-limiting example, in which:
-
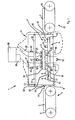
Figure 1 is a schematic frontal view of the apparatus during an operating configuration; -
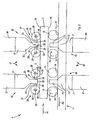
Figure 2 is a detail ofFigure 1 ; -
Figure 3 is a detail ofFigure 1 during a further operating configuration. - With reference to
Figure 1 , there is shown anapparatus 1 fordrying tiles 2. Theapparatus 1 comprisesfirst moving means 3 arranged for moving thetiles 2 towards adrying zone 4. The first moving means 3 comprises afirst belt 5 that supports and moves, thetiles 2 to thedrying zone 4 along an advance direction A1. - In an embodiment that is not shown, the first moving
means 3 may comprise a roller conveyor provided with a plurality of driven rollers that enable thetiles 2 to be supported and moved to thedrying zone 4. - The
apparatus 1 further comprises second moving means 43 arranged for moving thetiles 2 away from thedrying zone 4. The second moving means 43 comprises asecond belt 45 that supports and moves thetiles 2 away from thedrying zone 4 along the advance direction A1. - In an embodiment that is not shown, the second moving means 43 may comprise a roller conveyor provided with a plurality of driven rollers that enable the
tiles 2 to be supported and moved to thedrying zone 4. - In the
drying zone 4 there is third moving means 6, which receives thetile 2 from the first moving means 3. The third moving means 6 comprises a plurality ofrollers 8 rotatably supported by a frame 9 through supporting bars, which are not shown. In this way therollers 8 enable thetiles 2 to be supported and moved through thedrying zone 4. - The frame 9 further comprises a
first opening 10 placed at the entrance of thedrying zone 4 and a second opening 40 placed at the outlet of thedrying zone 4, further downstream than thefirst opening 10 according to the advance direction A1. - The third moving
means 6 is arranged near the first moving means 3 and the second moving means 43. In particular the third movingmeans 6 is interposed between the first movingmeans 3 and the second moving means 43 according to the advance direction A1. In this way therollers 8 of the third moving means 6 define, together with thefirst belt 5 and thesecond belt 45, an advance plane P for thetiles 2. Initially, thetile 2 is easily transferred from the first moving means 3 to the third moving means 6, and enters thedrying zone 4 through thefirst opening 10. Subsequently thetile 2 is transferred from the third moving means 6 to the second moving means 43 and exits thedrying zone 4 through thesecond opening 40. - The third moving means 6 further comprises a
strap 11 wound on a pair ofpulleys 12. The pair ofpulleys 12 supports thestrap 11 and the rotation of the pair ofpulleys 12 transmits motion to thestrap 11. Thestrap 11 comprises anactive part 13, which slides along a direction A2. - With reference to
Figure 2 , theactive part 13 of thestrap 11 interacts with aperipheral portion 14 of therollers 8. In thismanner rollers 8 are rotated according to a rotation direction R1 and support alower face 16 of thetiles 2 at aloading zone 15. In this manner thetiles 2 are thus supported and moved along the advance direction A1 owing to therollers 8. - The
apparatus 1 further comprises drying means 17, positioned in thedrying zone 4. The drying means 17 comprises asuction unit 18, that faces anupper face 19 of thetiles 2. The drying means 17 further comprises a blowingunit 20, that faces theupper face 19 of thetiles 2 in a position further downstream of thesuction unit 18 along the advance direction A1. - The
suction unit 18 extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of thetile 2 in this direction. In this way thesuction unit 18 is able to ensure suction along the entire width of thetile 2. - With reference to
Figure 2 , thesuction unit 18 has a section converging on the advance plane P, that has adistal region 21 with a greater section, anintermediate region 22 with a variable section and aproximal region 23 with a lesser section. Theproximal region 23 directly faces theupper face 19 of thetile 2 and finishes with alower end 25. - The blowing
unit 20 is structurally shaped like thesuction unit 18. The blowingunit 20 thus extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of thetile 2 in this direction. In this manner the blowingunit 20 is able to ensure blowing along the entire width of thetile 2. - The drying means 17 moves together with a positioning means 24. The positioning means 24 enables a constant distance D to be maintained between the
upper face 19 of thetiles 2 and thelower end 25 of the drying means 17. - The positioning means 24 comprises roller means 26 that is rotatably supported by the
drying means 17 by supportingbrackets 27. - The supporting
brackets 27 extend along the advance direction A1 and have afirst end 28 fixed near theproximal region 23 and asecond end 29 intended for rotatably supporting the roller means 26. The roller means 26 is thus at both sides of theproximal region 23, along the advance direction A1. - The roller means 26 defines an
interaction zone 30 at which the roller means 26 interacts with theupper face 19 of thetile 2 in transit and is induced to roll thereupon. - The
suction unit 18 is fixed to a supportingarm 31 by elastic connecting means that enables the suction means 18 to remain substantially in the same position with respect to the advance plane P when the supportingarm 31 performs rotations around anend 32 thereof, which is hinged on the frame 9 by further elastic connecting means. The elastic connecting means and the further elastic connecting means thus act as a hinge. - The supporting
arm 31 rotates around an axis Cl, that is perpendicular to the advance direction A1. - The blowing
unit 20 is fixed to a further supportingarm 33 through hinge means, that is not shown. The further supportingarm 33 is structurally and functionally shaped like the supportingarm 31. - The
suction unit 18 is connected to afirst suction conduit 37 and the blowingunit 20 is connected to a first blowingconduit 38. - The
apparatus 1 further comprises further drying means 67, positioned in thedrying zone 4 on the opposite side to the drying means 17 with respect to thetiles 2. The further drying means 67 comprises afurther suction unit 68 that faces thelower face 16 of thetiles 2. Thefurther suction unit 68 is arranged at thesuction unit 18 in the space betweenconsecutive rollers 8. - The
further suction unit 68 is structurally and functionally shaped like thesuction unit 18. Thefurther suction unit 68 then extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of thetile 2 in that direction. In this way thefurther suction unit 68 is able to ensure suction along the entire width of thetile 2. - The
suction unit 68 has a section converging on the advance plane P, and comprises a furtherdistal region 71 with a greater section, a furtherintermediate region 72 with a variable section and furtherproximal region 73 with a lesser section. The furtherupper region 73 faces thelower face 16 of thetile 2 directly. - The drying means 67 further comprises a
further blowing unit 70, that faces thelower face 16 of thetiles 2 in a position further downstream of thefurther suction unit 68 along the advance direction A1. - The
further blowing unit 70 is arranged at the blowingunit 20 at a lesser vertical height. - The
further blowing unit 70 is structurally shaped like theblowing unit 20. Thefurther blowing unit 70 thus extends along a direction that is transverse to the advance direction A1 by a length that is greater than the extent of thetile 2 in that direction. In this way the blowingunit 70 is able to ensure blowing along the entire width of thetile 2. - The further drying means 67 is fixed to the frame 9 through fixing means that is not shown. The further drying means 67 is arranged inside the drying
zone 4 so that the furtherupper region 73, which directly faces thelower face 16, is positioned in the gap left between twosuccessive rollers 8. Thefurther suction unit 68 is connected to asecond suction conduit 87 and thefurther blowing unit 70 is connected to asecond blowing conduit 88. - The
first suction conduit 37 and thesecond suction conduit 87 are connected to a main suction conduit, which is not shown, which is in turn connected to the inlet of the filter means 89. The filter means 89 receives from the main suction conduit the air, in which there is a small quantity of water that was removed from theupper face 19 and from thelower face 16 of thetiles 2. The filter means 89 thus separates the air from the water present, which is collected in a collecting vessel, which is not shown. - The filter means 89 is connected to fan means 90 through an inlet conduit, which is not shown.
- The fan means comprised the inlet conduit that is connected to the filter means 89 and a main blowing conduit, which is not shown.
- The fan means 90 further comprises a fan wheel, which is not shown, which is interposed between the inlet conduit and the main connecting conduit.
- The main blowing conduit is connected to the
first blowing conduit 38 and to thesecond blowing conduit 88. - Through the rotation of the fan wheel the fan means 90 creates the pressure that is necessary for receiving from the filter means 89 the air purified of any trace of water. The fan means 90 further blows air to the
blowing unit 20 and thefurther blowing unit 70. Initially, the air runs through the main blowing conduit and subsequently runs through thefirst blowing conduit 38 and thesecond blowing conduit 88. - The fan means 90 provides high-pressure air. This causes the air to heat, which promotes completion of the drying of the
tiles 2 by the blowingunit 20 and by thefurther blowing unit 70. - The fan means 90 thus ensures both suction of the air through the
suction unit 18 and thefurther suction unit 68 and blowing through the blowingunit 20 and thefurther blowing unit 70. - There can be applied a wear- and oxidation-resistant coating on the fan wheel on the fan means 90 so as to maintain the fan means 90 in a fully operational state.
-
Figure 3 shows an operating configuration X1 of theapparatus 1 in which thetile 2, which is in thedrying zone 4, has an irregular surface on theupper face 19. In particular, theupper face 19 showsflat portions 96 arranged at different vertical heights that alternate randomly and are joined together byoblique portions 97. - The positioning means 24 is in constant contact with the
upper face 19 through the roller means 26.Figure 3 shows thesuction unit 18 and the blowingunit 20, that are moved independently of one another, along a further direction A3 whilst the roller means 26 rolls on theupper face 19 following the profile thereof. Thesuction unit 18 and the blowingunit 20 face theflat portions 96, that are arranged at different vertical heights. In this way thesuction unit 18 and the blowingunit 20 ensure complete drying of theupper face 19 of thetile 2. - In another embodiment of the
apparatus 1, which is not shown, the drying means 17 and the further drying means 67 comprise blades made of rubber, mounted instead of the suction means 18 and/or of the blowing means 20. These blades differ from prior-art blades to be mounted on the supportingarms upper face 19. - In operation, initially the
wet tile 2 is supported and moved by the first moving means 3 to the dryingzone 4, along the advance direction A1. When thetile 2 reaches thefirst opening 10 of the frame 9 is transferred from the first moving means 3 to the third moving means 6, thus entering the dryingzone 4. As shown inFigure 1 , therollers 8 of the third moving means 6 thus support thetile 2 and make thetile 2 proceed along the advance direction A1. Drying starts when the most advanced edge of thetile 2 meets the first roller of the roller means 26 lifting the first roller and thus taking thesuction unit 18 to the envisaged height so as to maintain the distance D between theupper face 19 and thelower end 25 of thesuction unit 18 constant, whatever theflat portion 96 that thesuction unit 18 faces. - In a subsequent step, when the blowing
unit 20 faces theupper face 19 of thetile 2, the positioning means 24 of the blowingunit 20 forces the blowingunit 20 to be positioned at a precise vertical height. This vertical height is such as to maintain constant the distance D between theupper face 19 and thelower end 25 of the blowingunit 20, whatever theflat portion 96 that the blowingunit 20 faces. Simultaneously, the positioning means 24 of thesuction unit 18 continues to maintain thesuction unit 18 at a vertical height such as to maintain the distance D constant. This also occurs if the vertical height of theflat portion 96 that thesuction unit 18 faces, and the vertical height of theflat portion 96 that the blowingunit 20 faces, are different from one another. - In this way, whilst the
tile 2 passes through the dryingzone 4, the distance D between theupper face 19 and thelower end 25 is maintained constant. Optimal drying of theupper face 19 is thus ensured, as the drying means 17 can operate at an optimal distance from theupper face 19. - In another operating configuration which is not shown the
apparatus 1 is able to dry successively thetiles 2 that have different thicknesses. Also in this configuration the distance D between theupper face 19 and thelower end 25 is maintained constant as the positioning means 24 is maintained in contact with theupper face 19 whatever the value of the thickness of thetile 2.
Claims (20)
- Apparatus for drying tiles comprising moving means (6) suitable for supporting and moving said tiles (2) on a conveying plane (P) through a drying zone (4) provided with drying means (17), said drying means (17) being movable with respect to said conveying plane (P) so that when one of said tiles (2) to be dried is introduced into said drying zone (4), there is induced a suitable movement of said drying means (17), said drying means (17) comprising blowing means (20) constituted by a blowing unit (20) that faces an upper face (19) of the tiles (2), the apparatus being characterized in that said drying means (17) further comprise suction means (18) constituted by a suction unit (18) that faces the upper face (19) of the tiles (2), the blowing unit (20) being arranged in a position futher downstream of the suction unit (18) along the advance direction (A1) of the tiles (2), the blowing unit (20) being structurally shaped like the suction unit (18), said blowing unit (20) and said suction unit (18) both having a section converging on the advance plane (P) that has a distal region (21) with a greater section, an intermediate region (22) with a variable section and a proximal region (23) with a lesser section wherein the proximal region directly faces the upper face (19) of the tiles (2) and finishes with a lower end (25).
- Apparatus according to claim 1, wherein said drying means (17) is coupled with frame means (9) by oscillating means (31, 33).
- Apparatus according to claim 2, wherein said oscillating means comprises arm means (31, 33).
- Apparatus according to claim 3, wherein said arm means (31, 33) is coupled with said frame means (9) by hinge means.
- Apparatus according to claim 3, or 4, wherein said arm means (31, 33) is coupled with said drying means (17) by hinge means.
- Apparatus according to claim 4, or s, wherein said hinge means is elastic hinge means.
- Apparatus according to any preceding claim, wherein said drying means (17) is mounted on positioning means (24) arranged for positioning said drying means (17) with respect to said tiles (2).
- Apparatus according to claim 7, wherein said positioning means (24) is passive and is arranged on the crossing path of said tiles (2).
- Apparatus according to claim 8, wherein said positioning means (24) comprises roller means (26).
- Apparatus according to any preceding claim, wherein said drying means (17) comprises blades made of rubber.
- Apparatus according to any preceding claim, and further comprising further drying means (67).
- Apparatus according to claim 11, wherein said further drying means (67) is fixed relative to said frame means (9) and mounted on an opposite side of said drying means (17) with respect to said advance plane (F).
- Apparatus according to claim 11, or 12, wherein said further drying means (67) comprises further suction means (68).
- Apparatus according to claim 13, wherein said further drying means (67) comprises further blowing means (70).
- Apparatus according to any preceding claim, and further comprising fan means (90) associated with said drying means (17) and with said further drying means (67), if present.
- Apparatus according to claim 15, wherein said fan means (90) comprises a fan wheel provided with an antioxidant coating.
- Apparatus according to claim 15, wherein said fan means (90) is common to said suction means (18) and said blowing means (20).
- Apparatus according to claim 15 as appended to claim 14, wherein said fan means (90) is common to said further suction means (68) and to said further blowing means (70).
- Apparatus according to claim 14, wherein said further suction means (68) is structurally and functionally shaped like said suction unit (18), and said further blowing means (70) is structurally shaped like said blowing unit (20).
- Apparatus according to any preceding claim 15-18, wherein said fan means (90) provides high-pressure air causing the air to heat for promoting completion of the drying of the tiles.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL08737368T PL2137476T3 (en) | 2007-04-06 | 2008-04-02 | Apparatus for drying tiles |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT000127A ITMO20070127A1 (en) | 2007-04-06 | 2007-04-06 | APPARATUS FOR DRYING TILES |
| PCT/IB2008/000778 WO2008122855A2 (en) | 2007-04-06 | 2008-04-02 | Apparatus for drying tiles |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2137476A2 EP2137476A2 (en) | 2009-12-30 |
| EP2137476B1 true EP2137476B1 (en) | 2011-01-19 |
Family
ID=39831472
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP08737368A Not-in-force EP2137476B1 (en) | 2007-04-06 | 2008-04-02 | Apparatus for drying tiles |
Country Status (8)
| Country | Link |
|---|---|
| EP (1) | EP2137476B1 (en) |
| AT (1) | ATE496266T1 (en) |
| BR (1) | BRPI0809932A2 (en) |
| DE (1) | DE602008004636D1 (en) |
| ES (1) | ES2357880T3 (en) |
| IT (1) | ITMO20070127A1 (en) |
| PL (1) | PL2137476T3 (en) |
| WO (1) | WO2008122855A2 (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| ES2867598T3 (en) * | 2018-11-26 | 2021-10-20 | Upm Plywood Oy | A device and a method for drying a veneer, and a method for adapting a dryer to form a device for drying a veneer |
| CN110328775B (en) * | 2019-07-18 | 2024-04-05 | 南京汇科高分子材料有限公司 | A drying cabinet for producing glass is bordured and is used polyurethane combined material |
Family Cites Families (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR1121791A (en) * | 1954-04-14 | 1956-08-27 | Erich Kiefer | Drying process and installation |
| GB1511175A (en) * | 1975-10-17 | 1978-05-17 | Paterson Prod Ltd | Squeegee apparatus |
| US4700426A (en) * | 1982-09-28 | 1987-10-20 | Mcelroy Lucian G | Nozzle assembly for fluid stripping apparatus |
| JPS59122837A (en) * | 1982-12-28 | 1984-07-16 | Mitsubishi Electric Corp | Cleansing method of ventilating fan |
| US4589160A (en) * | 1984-06-11 | 1986-05-20 | Day David R | Apparatus for stripping fluids including dimensionally stable and substantially rigid bag |
| US4611409A (en) * | 1984-06-14 | 1986-09-16 | Fuji Photo Film Co., Ltd. | Liquid removing method |
| DE3708642C2 (en) * | 1987-03-17 | 1997-08-14 | Imas S P A | Device for the rapid drying of raw ceramic products, in particular tiles |
| JPH0613230Y2 (en) * | 1989-07-31 | 1994-04-06 | セントラル硝子株式会社 | Bending plate glass drainer |
| DE10163129C1 (en) * | 2001-12-20 | 2002-10-24 | Thomas Robert Metall Elektro | Device for drying moldings, especially ceramic moldings e.g. roof tiles, comprises a dry material support directly or indirectly supporting a molding on the lower side and provided with blow openings and suction openings |
-
2007
- 2007-04-06 IT IT000127A patent/ITMO20070127A1/en unknown
-
2008
- 2008-04-02 AT AT08737368T patent/ATE496266T1/en not_active IP Right Cessation
- 2008-04-02 DE DE602008004636T patent/DE602008004636D1/en active Active
- 2008-04-02 PL PL08737368T patent/PL2137476T3/en unknown
- 2008-04-02 BR BRPI0809932-4A2A patent/BRPI0809932A2/en not_active IP Right Cessation
- 2008-04-02 EP EP08737368A patent/EP2137476B1/en not_active Not-in-force
- 2008-04-02 WO PCT/IB2008/000778 patent/WO2008122855A2/en not_active Ceased
- 2008-04-02 ES ES08737368T patent/ES2357880T3/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| EP2137476A2 (en) | 2009-12-30 |
| PL2137476T3 (en) | 2011-05-31 |
| ES2357880T3 (en) | 2011-05-03 |
| WO2008122855A3 (en) | 2009-04-09 |
| ITMO20070127A1 (en) | 2008-10-07 |
| DE602008004636D1 (en) | 2011-03-03 |
| BRPI0809932A2 (en) | 2014-10-07 |
| ATE496266T1 (en) | 2011-02-15 |
| WO2008122855A2 (en) | 2008-10-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| TWI469865B (en) | Device for conveying and folding blanks | |
| EP1964795B1 (en) | Device for cleaning from a conveyor belt fluid substances sprayed thereon | |
| WO2003099461A1 (en) | Apparatus and method for painting objects such as profiles, panels or suchlike | |
| US3924397A (en) | Apparatus for removing impurities from fibrous material | |
| CA2371552C (en) | Method for drying veneer and corresponding drying device | |
| DK2861356T3 (en) | coating lines | |
| CN118321300A (en) | A cleaning device for glass warping detection and use method thereof | |
| KR200475663Y1 (en) | Sand blast machine | |
| KR20130001190A (en) | Processing apparatus for vegetables | |
| US20110232239A1 (en) | Device for transporting objects | |
| WO2008122855A2 (en) | Apparatus for drying tiles | |
| KR101320126B1 (en) | Apparatus for preventing upward movement of strip | |
| US6672202B2 (en) | Device for flattening pieces of meat | |
| CN104528419A (en) | Detection unit for online negative pressure air suction conveying device of roll paper die-cutting machine belt | |
| US5919023A (en) | Compact overhead conveyor | |
| CN115922527A (en) | A self-adaptive double-roller derusting equipment | |
| KR102631892B1 (en) | Remove fruit hairs Devices | |
| CN210368295U (en) | Water-drop-proof steam drying cylinder drying machine | |
| JP2009119737A (en) | Agricultural multi-sheet processing equipment | |
| CN117565283A (en) | A latex glove drying and unloading device | |
| CN214132430U (en) | Panel surface treatment device for furniture | |
| KR102125711B1 (en) | Processing apparatus for thin metal plate | |
| EP3619033B1 (en) | Rotary tablet press with an outlet device | |
| JPH0566086A (en) | Sheet treatment device using caterpillar | |
| CN214747079U (en) | A drying device for machining mechanical parts |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20091008 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20100210 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MT NL NO PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 602008004636 Country of ref document: DE Date of ref document: 20110303 Kind code of ref document: P |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602008004636 Country of ref document: DE Effective date: 20110303 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2357880 Country of ref document: ES Kind code of ref document: T3 Effective date: 20110503 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20110119 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20110119 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110419 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110519 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110519 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110420 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110419 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110430 |
|
| 26N | No opposition filed |
Effective date: 20111020 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20111230 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111101 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110502 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602008004636 Country of ref document: DE Effective date: 20111020 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602008004636 Country of ref document: DE Effective date: 20111101 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110402 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 496266 Country of ref document: AT Kind code of ref document: T Effective date: 20110119 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20120402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120402 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120430 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20110402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110119 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20140324 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 20150427 Year of fee payment: 8 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: PL Payment date: 20150318 Year of fee payment: 8 Ref country code: IT Payment date: 20150423 Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160402 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160403 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20181205 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20160402 |