EP1954424B1 - Einteiliger stahlkolben als feinguss-variante mit kern für die feingusstechnische herstellung eines kühlkanales - Google Patents
Einteiliger stahlkolben als feinguss-variante mit kern für die feingusstechnische herstellung eines kühlkanales Download PDFInfo
- Publication number
- EP1954424B1 EP1954424B1 EP06818435A EP06818435A EP1954424B1 EP 1954424 B1 EP1954424 B1 EP 1954424B1 EP 06818435 A EP06818435 A EP 06818435A EP 06818435 A EP06818435 A EP 06818435A EP 1954424 B1 EP1954424 B1 EP 1954424B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- casting
- cooling channel
- steel piston
- piston
- precision
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000001816 cooling Methods 0.000 title claims abstract description 31
- 229910000831 Steel Inorganic materials 0.000 title claims abstract description 30
- 239000010959 steel Substances 0.000 title claims abstract description 30
- 238000005495 investment casting Methods 0.000 title claims abstract description 11
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 10
- 238000005266 casting Methods 0.000 claims abstract description 30
- 238000000034 method Methods 0.000 claims abstract description 12
- 238000002485 combustion reaction Methods 0.000 claims abstract description 9
- 239000002826 coolant Substances 0.000 claims description 10
- 239000011162 core material Substances 0.000 description 14
- 239000000919 ceramic Substances 0.000 description 3
- 238000007528 sand casting Methods 0.000 description 3
- 239000000463 material Substances 0.000 description 2
- 238000007711 solidification Methods 0.000 description 2
- 230000008023 solidification Effects 0.000 description 2
- 229910000838 Al alloy Inorganic materials 0.000 description 1
- 229910001018 Cast iron Inorganic materials 0.000 description 1
- 229910001208 Crucible steel Inorganic materials 0.000 description 1
- 229910001141 Ductile iron Inorganic materials 0.000 description 1
- CWYNVVGOOAEACU-UHFFFAOYSA-N Fe2+ Chemical compound [Fe+2] CWYNVVGOOAEACU-UHFFFAOYSA-N 0.000 description 1
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical group [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 1
- 229910001296 Malleable iron Inorganic materials 0.000 description 1
- 238000010276 construction Methods 0.000 description 1
- 239000000835 fiber Substances 0.000 description 1
- 230000017525 heat dissipation Effects 0.000 description 1
- 210000003734 kidney Anatomy 0.000 description 1
- 229910052751 metal Inorganic materials 0.000 description 1
- 239000002184 metal Substances 0.000 description 1
- 239000011819 refractory material Substances 0.000 description 1
- 239000004576 sand Substances 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images
Classifications
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F3/00—Pistons
- F02F3/16—Pistons having cooling means
- F02F3/20—Pistons having cooling means the means being a fluid flowing through or along piston
- F02F3/22—Pistons having cooling means the means being a fluid flowing through or along piston the fluid being liquid
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C7/00—Patterns; Manufacture thereof so far as not provided for in other classes
- B22C7/02—Lost patterns
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22C—FOUNDRY MOULDING
- B22C9/00—Moulds or cores; Moulding processes
- B22C9/02—Sand moulds or like moulds for shaped castings
- B22C9/04—Use of lost patterns
-
- F—MECHANICAL ENGINEERING; LIGHTING; HEATING; WEAPONS; BLASTING
- F02—COMBUSTION ENGINES; HOT-GAS OR COMBUSTION-PRODUCT ENGINE PLANTS
- F02F—CYLINDERS, PISTONS OR CASINGS, FOR COMBUSTION ENGINES; ARRANGEMENTS OF SEALINGS IN COMBUSTION ENGINES
- F02F2200/00—Manufacturing
- F02F2200/06—Casting
Definitions
- the invention relates to a method for producing a one-piece steel piston for an internal combustion engine of a passenger car and a steel piston produced by this method according to the features of the preamble of claim 1.
- one-piece steel pistons with a closed cooling channel are already known, which are manufactured in the sand casting process.
- the wall thicknesses in the sand casting method and the chill casting are significantly higher than in precision casting, so that a desired lightweight construction in the car sector can not be realized.
- the DE 38 02 714 A1 discloses a two-piece internal combustion engine piston having a head portion of ferrous metal or an aluminum alloy and having a piston stem spaced away from the head portion and connected by a pivot pin to a pair of support bosses attached to bottom of support members projecting from the head portion are, wherein the head part is provided with a closed circular cross-section cooling channel in the region between the ring belt and the combustion chamber of the piston.
- the head part is designed as a steel part or spheroidal cast iron or malleable cast iron part produced by precision casting, sand casting or shell casting steel part or nodular cast iron.
- Aüs of gattüngssentenden US-A-4,428,330 the features of the preamble of Patentauspriches 1 are known.
- the invention is therefore based on the object to provide a steel piston in particular for the operation of high-speed and high-pressure diesel engines, which meets the above-mentioned parameters, in particular lowered the exhaust emissions during operation of the piston and at the same time with a performance increase lower consumption of the engine is achieved, whereby the production costs for such a steel piston are to be considered.
- a production method in which the casting method is and will thus be the advantage that, on the one hand, a higher-strength material, in particular steel, is used and, on the other hand, the cooling channel, in particular its cross-section, is increased.
- the larger surface the cooling channel increases the heat dissipation and reduces the heat load of the critical areas on the steel piston, in particular in the region of the piston crown.
- the mechanical properties of the steel and the greater potential of the investment casting process counteract the design freedom of the increased load.
- the novelty of the invention relates to the realization of a one-piece steel piston of a highly loaded, future-oriented steel piston for the operation of fast-running high-pressure diesel engines, which is manufactured by investment casting and in which, if necessary, the closing of the cooling channel can be done, but not
- it is a core, especially a core of high temperature resistant materials, in particular a ceramic core, which can be removed in a simple and fast manner according to the present invention from the cast steel piston.
- the invention relates to a cast one-piece steel piston, in which the removal of the core for the cooling channel, in particular of the ceramic core, is done in an economical manner, in particular leads to a cost reduction.
- a plurality of openings with any sufficient cross-section in particular kidney-shaped or similar openings with a sufficient cross-section, are provided in the casting, which are closed form-fit or material-locking after removal of the core.
- the oil inlet or oil outlet bore can already be integrated by suitable manufacturing process in the closing component.
- the casting mold is designed to hold the lost core via sleeves or the like.
- the entire steel piston can be poured very quickly and easily by investment casting, with just as quickly and easily the lost core can be removed after the solidification of the casting melt.
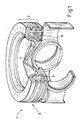
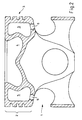
- FIGS. 1 and 2 show a section through a one-piece steel piston 1, and on the other hand, a three-dimensional view of such a piston, which has been produced by investment casting. It can be seen that in the piston head 2, in particular behind a ring field 3 with a plurality of annular grooves and a combustion bowl 4 extending, a preferably radially encircling cooling channel 5 is present, which has been produced by means of a core, in particular a sand, ceramic and / or fiber-containing core.
- the piston 1 in a conventional manner piston stems and bolt holes, which are arranged below the piston crown 2.
- piston stems and bolt holes which are arranged below the piston crown 2.
- Such exemplary but non-limiting embodiment is in the FIGS. 1 and 2 shown.
- At least one closure part 6, in particular a plurality of closure parts 6, is provided, which have a round, oval, kidney or other geometric shape, which or after the casting of the piston 1 in the through the casting mold and the lost Core formed connection to the cooling channel 5 is (are) used.
- these closure parts 6 are not used in all connections, so that then at least one oil inlet and at least one oil outlet bore or opening is available.
- the cavity is not used for a circulating cooling medium, but for weight savings.
- a negative mold which images the later outer contours of the piston blank to be cast, made of a refractory material.
- the core material is fixed at a distance to this form via pins, sleeves or the like, and the negative Fm is filled with casting melt.
- the negative mold is removed, so that serve as inlet or discharge openings for the cooling channel to be removed pins, quills and the like. After these have been removed, as well as the core material, the at least one closure part is introduced into the opening to close the cooling channel.
- the respective closure part can be non-positively and / or positively attached to the underside of the cooling channel or elsewhere, where the holder for the core material have been found attached.
- the closure part it is conceivable to at least a place where the opening has arisen after casting, no closure part to install, so as to realize the inlet or drain hole.
- the closure member 6 can be seen, which is inserted into the opening formed after the casting of the steel piston.
- the resulting during casting opening extends in an advantageous manner with respect to the piston stroke down, since from this direction usually the cooling medium (cooling oil) is injected.
- the invention provides that the resulting during casting openings are present in the cooling channel 5 radially circumferentially at several points below the cooling channel 5, that means that such openings are only partially available. That is, the cooling channel 5 is closed at its bottom after casting, but two or more openings are present. These openings are used as inlet and outlet opening for the cooling medium. If more than two such openings are present, they can also serve as inlet or outlet opening for the cooling medium.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Physics & Mathematics (AREA)
- Fluid Mechanics (AREA)
- Chemical & Material Sciences (AREA)
- Combustion & Propulsion (AREA)
- General Engineering & Computer Science (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
- Pistons, Piston Rings, And Cylinders (AREA)
Description
- Die Erfindung betrifft ein Verfahren zur Herstellung eines einteiligen Stahlkolbens für eine Brennkraftmaschine eines Personenkraftwagens sowie einen nach diesem Verfahren hergestellten Stahlkolben gemäß den Merkmalen des Oberbegriffes des Patentanspruches 1.
- Bekannt sind Stahlkolben, die allerdings im Bereich von Nutzkraftfahrzeugen serienmäßig eingesetzt wurden, da hier das Gewicht von Stahlkolben keine so große Rolle spielt wie bei Verbrennungsmotoren mit dem gegenüber kleineren Kolben im Personenkraftwagenbereich. Bei den bekannten Stahlkolben wurde ein Kühlkanal im Kolbenboden (auch Kolbenkopf genannt) offen gestaltet, wobei das Verschlieβen des Kühlkanales durch ein zusätzliches ein- oder mehrteiliges Element, wie zum Beispiel ein geteilter Ring, mit Hilfe von diversen Verbindungstechniken wie zum Beispiel Laserschweißen durchgeführt wurde. Durch diese zusätzlichen Fertigungs- und Montageschritte entstehen in nachteiliger Weise Mehrkosten.
- Dem gegenüber sind schon einteilige Stahlkolben mit geschlossenem Kühlkanal bekannt, die im Sandguss-Verfahren hergestellt werden. Die Wandstärken im Sandguss-Gießverfahren und beim Kokillenguß sind jedoch deutlich höher als im Feinguss, so dass sich ein im PKW-Bereich gewünschter Leichtbau nicht realisieren lässt.
- Bei modernen Brennkraftmaschinen ist eine fortlaufende Leistungssteigerung gewünscht, bei der aufgrund immer strengerer Auflagen von Gesetzgebern bezüglich der Abgasemissionen diese Emissionen gesenkt, zum anderen auf Wunsch der Kunden nach leistungsstärkeren Aggregaten ein weiter geringerer Verbrauch zu
- die Merkmale des Oberbegriffes des Patentansprüches 1 bekannt.
- erzielen ist. Zur Erfüllung zumindest dieser beiden Forderungen, die sich in der Praxis widersprechen, führt die Verringerung der Abgasemissionen einerseits und die Leistungssteigerung andererseits zu einer höheren thermischen und mechanischen Belastung des Kolbens für Dieselbrennkraftmaschinen. Diese Belastungen steigen mit den dann herrschenden Zünddrücken und Drehzahlen an.
- Die
DE 38 02 714 A1 offenbart einen zweitteiligen Kolben für Brennkraftmaschinen, mit einem Kopfteil aus Eisenmetall oder einer Aluminium-Legierung und mit einem Kolbenschaft, der in einem Abstand vom Kopfteil entfernt angeordnet und mittels eines Anlenkzapfens mit einem Paar von Tragaugen verbunden ist, die unten an vom Kopfteil vorstehenden Stützgliedern angebracht sind, wobei das Kopfteil mit einem im Querschnitt geschlossenen ringförmig umlaufenden Kühlkanal im Bereich zwischen Ringgürtel und Brennraum des Kolbens versehen ist. Zur Herstellung des Kopfteiles wird angegeben, dass das Kopfteil als ein durch Präzisionsguss, Sandformguss oder Schalenguss hergestelltes Stahlteil bzw. Sphäroguss hergestelltes Stahlteil bzw. Sphäroguss- oder Temperguss-Teil ausgeführt ist. Aüs des gattüngsbildendenUS-A-4 428 330 sind die Merkmale des Oberbegriffes des Patentauspriches 1 bekannt. - Der Erfindung liegt daher die Aufgabe zugrunde, einen Stahlkolben insbesondere für den Betrieb von schnell laufenden und hoch belasteten Dieselmotoren bereitzustellen, der die eingangs geschilderten Parameter erfüllt, bei dem insbesondere die Abgasemissionen im Betrieb des Kolbens gesenkt und gleichzeitig bei einer Leistungssteigerung ein geringerer Verbrauch der Brennkraftmaschine erzielt wird, wobei auch die Herstellungskosten für einen solchen Stahlkolben zu beachten sind.
- Diese Aufgabe ist durch die Merkmale des Patentanspruches 1 gelöst
- Erfindungsgemäß ist ein Herstellungsyerfahren vorgesehen, bei dem das Gießverfahren ein Feingussverfahren ist und wird Hierdurch bleibt zunächst der Vorteil bestehen, dass zum einen ein höher festerer Werkstoff, insbesondere Stahl, zum Einsatz kommt und zum anderen der Kühlkanal, insbesondere dessen Querschnitt, vergrößert wird. Die größere Oberfläche des Kühlkanales erhöht die Wärmeabfuhr und reduziert die Wärmebelastung der kritischen Bereiche am Stahlkolben, insbesondere im Bereich des Kolbenbodens. Die mechanischen Eigenschaften des Stahls und das größere Potenzial des Feinguss-Verfahrens, wirken bezüglich der Gestaltungsfreiheit der erhöhten Belastung entgegen. Damit bezieht sich die Neuheit der Erfindung auf die Realisierung eines einteiligen Stahlkolbens eines hoch belasteten, zukunftsorientierten Stahlkolbens für den Betrieb von schnell laufenden hoch belasteten Dieselmotoren, der im Feinguss-Verfahren hergestellt wird und bei dem ggfs. das Verschließen des Kühlkanals erfolgen kann, aber nicht muß.. Insbesondere geht es um einen Kern, vor allen Dingen einen Kern aus hochtemperaturfesten Werkstoffen, insbesondere einen Keramikkern, der auf einfache und schnelle Art und Weise gemäß der vorliegenden Erfindung aus dem gegossenen Stahlkolben entfernt werden kann. Damit betrifft die Erfindung einen gegossenen einteiligen Stahlkolben, bei dem das Entfernen des Kernes für den Kühlkanal, insbesondere des Keramikkerns, auf eine wirtschaftliche Art und Weise geschieht, insbesondere die zu einer Kostenreduzierung führt. Hierzu werden mehrere Öffnungen mit beliebigem ausreichendem Querschnitt, insbesondere nierenförmige oder ähnliche Öffnungen mit einem ausreichenden Querschnitt, in dem Gussteil vorgesehen, die nach dem Entfernen des Kerns form- oder stoffschlüssig verschlossen werden. Dabei kann in dem verschlieβenden Bauteil bereits die Öleintritts- bzw. Ölaustrittsbohrung durch geeignetes Fertigungsverfahren integriert sein.
- In Weiterbildung der Erfindung ist vorgesehen, dass die Gießform dazu ausgebildet ist, den verlorenen Kern über Pinolen oder dergleichen zu halten. Damit kann der gesamte Stahlkolben sehr schnell und einfach im Feinguss-Verfahren gegossen werden, wobei ebenso schnell und einfach der verlorene Kern nach dem Erstarren der Gießschmelze entfernt werden kann.
- Die beiden
Figuren 1 und2 zeigen einerseits einen Schnitt durch einen einteiligen Stahlkolben 1, und andererseits eine dreidimensionale Ansicht eines solchen Kolbens, der im Feinguss-Gießverfahren hergestellt worden ist. Hierbei ist erkennbar, dass im Kolbenboden 2, insbesondere hinter einem Ringfeld 3 mit mehreren Ringnuten und einer Brennraummulde 4 verlaufend, ein vorzugsweise radial umlaufender Kühlkanal 5 vorhanden ist, der mittels eines Kernes, insbesondere eines sand-, keramik- und/oder faserhaltigen Kernes, hergestellt worden ist. Außerdem weist der Kolben 1 in an sich bekannter Weise Kolbenschäfte und Bolzenbohrungen auf, die unterhalb des Kolbenbodens 2 angeordnet sind. Eine derartige beispielhafte, aber nicht einschränkende Ausgestaltung ist in denFiguren 1 und2 gezeigt. - Nach dem Gießen des Kolbens 1 wird zumindest ein Verschlussteil 6, insbesondere mehrere Verschlussteile 6, vorgesehen, die eine runde, ovale, nieren- oder andere geometrische Form aufweisen, das oder die nach dem Gießen des Kolbens 1 in die durch die Gießform und den verlorenen Kern gebildete Verbindung zu dem Kühlkanal 5 eingesetzt wird (werden). Diese Verschlußteile 6 werden aber nicht in alle Verbindungen eingesetzt, so dass dann zumindest eine Öleintritts- und zumindest eine Ölaustrittsbohrung bzw. -Öffnung zur Verfügung steht. Daneben ist es selbstverständlich auch denkbar, dass der Hohlraum nicht für ein zirkulierendes Kühlmedium, sondern zur Gewichtsersparnis genutzt wird.
- Bei dem konkreten Ausführungsbeispiel, mit dem die in den
Figuren 1 und2 gezeigten Kolben hergestellt werden, handelt es sich also um das Feinguss-Verfahren. Bei diesem Verfahren wird eine Negativ-Form, die die späteren äußeren Konturen des zu gießenden Kolbenrohlings abbildet, aus einem hitzebeständigen Material hergestellt. Dabei wird in erfindungsgemäßer Weise an dieser Form über Stifte, Pinolen oder dergleichen das Kernmaterial auf Distanz befestigt und die Negativ-F m mit Gießschmelze gefüllt. Nachdem Erstarren der Gießschmelze wird die Negativ-Form entfernt, so dass als Zulauf bzw. Ablauföffnungen für den Kühlkanal die zu entfernenden Stifte, Pinolen und dergleichen dienen. Nachdem auch diese entfernt worden sind, genauso wie das Kernmaterial, wird das zumindest eine Verschlussteil in die Öffnung eingebracht, um den Kühlkanal zu verschließen. Das jeweilige Verschlussteil kann kraft- und/oder formschlüssig an der Unterseite des Kühlkanales oder an anderer Stelle, an der sich die Halterung für das Kernmaterial befunden haben, angebracht werden. Ergänzend oder alternativ zu dem Verschlussteil ist es denkbar, an die zumindest eine Stelle, an der nach dem Gießen die Öffnung entstanden ist, kein Verschlussteil anzubringen, um damit die Zulauf oder Ablaufbohrung zu realisieren. - In
Figur 2 ist noch einmal das Verschlussteil 6 erkennbar, das in die Öffnung, die nach dem Gießen des Stahlkolbens entsteht eingesetzt wird. Die beim Gießen entstehende Öffnung erstreckt sich in vorteilhafter Weise in Bezug auf die Kolbenhubachse nach unten, da aus dieser Richtung im Regelfall das Kühlmedium (Kühlöl) eingespritzt wird. Die Erfindung sieht vor, dass die beim Gießen entstehenden Öffnungen in dem Kühlkanal 5 radial umlaufend an mehreren Stellen unterhalb des Kühlkanales 5 vorhanden sind, dass bedeutet das solche Öffnungen nur abschnittsweise vorhanden sind. Das heißt, dass der Kühlkanal 5 an seiner Unterseite nach dem Gießen verschlossen ist, jedoch zwei oder mehr Öffnungen vorhanden sind. Diese Öffnungen werden als Zulauf und Ablauföffnung für das Kühlmedium genutzt. Sind mehr als zwei solcher Öffnungen vorhanden, können diese ebenfalls als Zulauf oder Ablauföffnung für das Kühlmedium dienen. Daneben ist es denkbar, sämtliche Öffnungen mit dem Verschlussteil 6 zu verschließen, bis auf zumindest eine Zulauf und zumindest eine Ablauföffnung für das Kühlmedium. Außerdem ist es denkbar, dass sämtliche nach dem Gießen vorhanden Öffnungen in dem Kühlkanal 5 von einem Verschlussteil 6 verschlossen ist, so dass danach der Kühlkanal 5 komplett verschlossen ist. Um den Zulauf und den Ablauf für das Kühlmedium zu realisieren kann dann entweder an anderer Stelle (neben der durch das Verschlussteil 6 verschlossenen Öffnung zu mindest eine Zulauf und Ablauföffnung für das Kühlmedium) eingebracht, insbesondere gebohrt werden. Weiterhin ist es denkbar, dass das Verschlussteil 6 seinerseits eine Öffnung aufweist, die dann als Zulauf oder Ablauf für das Kühlmedium dient.
Claims (6)
- Verfahren zur Herstellung eines einteiligen Stahlkolbens einer Brennkraftmaschine eines Personenkraftwagens, wobei der Stahlkolben in einem Gießverfahren unter Verwendung einer die äußeren Konturen des Stahlkolbens bildende Gießform hergestellt und nach dem Gießen fertig bearbeitet wird, wobei zur Realisierung eines Kühlkanales ein verlorener Kern eingesetzt wird, wobei die Gießform und der verlorene Kern so gestaltet sind, dass zumindest zwei oder mehr Öffnungen in dem Kühlkanal entstehen, nachdem die Gießform und der verlorene Kern entfernt worden sind, dadurch gekennzeichnet, dass das Gießverfahren ein Feingussverfahren ist und
, zumindest eine Öffnung des Kühlkanales mit einem Verschlussteil verschlossen wird. - Verfahren nach Anspruch 1, dadurch gekennzeichnet, dass die Gießform dazu ausgebildet ist, den verlorenen Kern über Pinolen zu halten.
- Stahlkolben (1) mit einem Kühlkanal (5), gekennzeichnet durch seine Herstellung nach dem Verfahren nach einem der vorhergehenden Ansprüche, wobei zumindest eine Öffnung des Kühlkanales mit einem Verschlussteil verschlossen ist.
- Stahlkolben (1) nach Anspruch 3, dadurch gekennzeichnet, dass das Verschlussteil (6) für die zumindest eine Öffnung des Kühlkanales (5) oval- oder nierenförmig ausgebildet ist.
- Stahlkolben (1) nach Anspruch 3 oder 4, dadurch gekennzeichnet, dass das Verschlussteil (6) Kraft- und/oder Formschlüssig in die zumindest eine Öffnung des Kühlkanales (5) eingesetzt ist.
- Stahl kolben (1) nach einem der Ansprüche 3 bis 5, dadurch gekennzeichnet, dass das Verschlussteil (6) eine Öffnung für einen Zulauf- oder Ablauf eines Kühlmediums in den Kühlkanal (5) hinein oder aus dem Kühlkanal (5) heraus aufweist.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| DE102005053999 | 2005-11-10 | ||
| PCT/EP2006/010737 WO2007054299A1 (de) | 2005-11-10 | 2006-11-09 | Einteiliger stahlkolben als feinguss-variante mit kern für die feingusstechnische herstellung eines kühlkanales |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP1954424A1 EP1954424A1 (de) | 2008-08-13 |
| EP1954424B1 true EP1954424B1 (de) | 2011-08-10 |
Family
ID=37667196
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP06818435A Not-in-force EP1954424B1 (de) | 2005-11-10 | 2006-11-09 | Einteiliger stahlkolben als feinguss-variante mit kern für die feingusstechnische herstellung eines kühlkanales |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP1954424B1 (de) |
| AT (1) | ATE519551T1 (de) |
| WO (1) | WO2007054299A1 (de) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102011116332A1 (de) * | 2011-07-05 | 2013-01-10 | Mahle International Gmbh | Kolben für einen Verbrennungsmotor |
| CN103394642A (zh) * | 2013-07-19 | 2013-11-20 | 宁波吉威熔模铸造有限公司 | 一种汽车发动机活塞的铸造方法 |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| BR8700642A (pt) * | 1987-02-09 | 1988-08-30 | Metal Leve Sa | Embolo articulado |
| JP3915155B2 (ja) * | 1996-12-17 | 2007-05-16 | アイシン精機株式会社 | 内燃機関用ピストンの製造方法 |
-
2006
- 2006-11-09 WO PCT/EP2006/010737 patent/WO2007054299A1/de not_active Ceased
- 2006-11-09 EP EP06818435A patent/EP1954424B1/de not_active Not-in-force
- 2006-11-09 AT AT06818435T patent/ATE519551T1/de active
Also Published As
| Publication number | Publication date |
|---|---|
| EP1954424A1 (de) | 2008-08-13 |
| ATE519551T1 (de) | 2011-08-15 |
| WO2007054299A1 (de) | 2007-05-18 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| DE102014101080B3 (de) | Vorrichtung zur Herstellung eines Zylinderkurbelgehäuses im Niederdruck- oder Schwerkraftgießverfahren | |
| DE202007018797U1 (de) | Gießform zum Gießen eines Gussteils und Verwendung einer solchen Gießform | |
| EP3334918B1 (de) | Kolben für eine brennkraftmaschine | |
| DE102007044105A1 (de) | Gießkern zur Bildung eines Kühlkanals in einem gießtechnisch hergestellten Kolben | |
| EP1922479B1 (de) | Kolben für eine brennkraftmaschine | |
| WO2010003398A1 (de) | Einlegeteil für einen kolben eines verbrennungsmotors sowie mit dem einlegeteil versehener kolben oder kolbenkopf | |
| DE102008055848A1 (de) | Kühlkanalkolben einer Brennkraftmaschine mit einem Verschlusselement, das den Kühlkanal verschließt | |
| DE102012203570A1 (de) | Gegossener Leichtmetallkolben, insbesondere ein Aluminiumkolben | |
| EP0937888A2 (de) | Verfahren zur Herstellung eines Kolbens für Brennkraftmaschinen | |
| EP1819920B1 (de) | Kolben für einen verbrennungsmotor | |
| WO2007076811A2 (de) | Kolben für einen verbrennungsmotor | |
| EP3377244B1 (de) | Gegossene zu- und ablauföffnungen bei stahlguss- und eisen-gusskolben | |
| DE10129046B4 (de) | Kolben für eine Brennkraftmaschine mit einem Eingußkörper | |
| DE102008031864A1 (de) | Einlegteil für einen Kolben eines Verbrennungsmotors sowie mit dem Einlegeteil versehener Kolben oder Kolbenkopf | |
| EP2734322B1 (de) | GIEßKERN EINER GUSSFORM ZUR HERSTELLUNG EINES ZYLINDERS | |
| EP3807514A1 (de) | Gegossener kolben für einen verbrennungsmotor, aus einem material auf eisenbasis | |
| EP3926158B1 (de) | Verfahren zur herstellung eines kolbens | |
| EP1954424A1 (de) | Einteiliger stahlkolben als feinguss-variante mit kern für die feingusstechnische herstellung eines kühlkanales | |
| EP3068560B1 (de) | Komplexes gussbauteil sowie giessverfahren hierfür | |
| DE19954725A1 (de) | Kolben mit einer Verbindung von einem Kühlkanal zu einer Kolbenbolzenbohrung | |
| DE102014210875A1 (de) | Kolben und Verfahren zu dessen Herstellung | |
| DE102004040539B4 (de) | Zylinder-Kurbelgehäuse für eine Mehrzylinder-Hubkolbenmaschine sowie Verfahren zur Herstellung eines Zylinder-Kurbelgehäuses für eine Mehrzylinder-Hubkolbenmaschine | |
| EP2165789B1 (de) | Verfahren zur Herstellung eines Kolbens einer Brennkraftmaschine mit einem mehrteiligen Kernschieber | |
| DE102008031862A1 (de) | Einlegeteil für einen Kolben eines Verbrennungsmotors sowie mit dem Einlegeteil versehener Kolben oder Kolbenkopf | |
| DE10121861B4 (de) | Aus Leichtmetallwerkstoff gegossenes Motorelement und Verstärkungselement |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20080404 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20090218 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| DAX | Request for extension of the european patent (deleted) | ||
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU LV MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D Free format text: NOT ENGLISH |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D Free format text: LANGUAGE OF EP DOCUMENT: GERMAN |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 502006010011 Country of ref document: DE Effective date: 20111006 |
|
| RIN2 | Information on inventor provided after grant (corrected) |
Inventor name: BUERKLE, GUNTER Inventor name: GNIESMER, VOLKER Inventor name: OTTLICZKY, EMMERICH Inventor name: WEIMAR, HANS-JOACHIM Inventor name: REHL, ANDREAS Inventor name: SCHALLER, CHRISTIAN |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: VDEP Effective date: 20110810 |
|
| LTIE | Lt: invalidation of european patent or patent extension |
Effective date: 20110810 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111212 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111210 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111111 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FD4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: IE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 |
|
| BERE | Be: lapsed |
Owner name: KS KOLBENSCHMIDT G.M.B.H. Effective date: 20111130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| 26N | No opposition filed |
Effective date: 20120511 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111130 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 502006010011 Country of ref document: DE Effective date: 20120511 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 519551 Country of ref document: AT Kind code of ref document: T Effective date: 20111109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111109 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20121130 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20121120 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111121 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20111109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20111110 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20110810 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20131109 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20140731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131109 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20131202 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20221123 Year of fee payment: 17 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 502006010011 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240601 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20240601 |