EP1619012B1 - Pellet machine with oleodynamic control extruder group - Google Patents
Pellet machine with oleodynamic control extruder group Download PDFInfo
- Publication number
- EP1619012B1 EP1619012B1 EP05425162A EP05425162A EP1619012B1 EP 1619012 B1 EP1619012 B1 EP 1619012B1 EP 05425162 A EP05425162 A EP 05425162A EP 05425162 A EP05425162 A EP 05425162A EP 1619012 B1 EP1619012 B1 EP 1619012B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- extruder
- pressure roller
- oleodynamic
- pellet machine
- machine according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000008188 pellet Substances 0.000 title claims description 19
- 239000002023 wood Substances 0.000 claims description 6
- 239000000463 material Substances 0.000 description 9
- 238000001125 extrusion Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 238000003825 pressing Methods 0.000 description 2
- 230000004913 activation Effects 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 239000012530 fluid Substances 0.000 description 1
- 230000001050 lubricating effect Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 230000002093 peripheral effect Effects 0.000 description 1
- 239000002994 raw material Substances 0.000 description 1
- 230000001105 regulatory effect Effects 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B30—PRESSES
- B30B—PRESSES IN GENERAL
- B30B11/00—Presses specially adapted for forming shaped articles from material in particulate or plastic state, e.g. briquetting presses, tabletting presses
- B30B11/20—Roller-and-ring machines, i.e. with roller disposed within a ring and co-operating with the inner surface of the ring
- B30B11/201—Roller-and-ring machines, i.e. with roller disposed within a ring and co-operating with the inner surface of the ring for extruding material
- B30B11/208—Roller constructions; Mounting of the rollers
Definitions
- This invention concerns vertical, cylindrical extruder pellet machines in general with internal pressure rollers, and refers in particular to an extruder group for such machines.
- the machines taken into consideration here and used for pelletising wood usually include a rotating annular extruder, having a large number of radial holes and pressing rollers, also turning, positioned and operating at a tangent to the inner surface of the perforated extruder.
- the starting raw material to be made into pellets is forwarded and crushed between the pressure rollers and the inner surface of the extruder and forced, in this way, to be extruded through the holes in the die.
- the pressure rollers are usually knurled to increase the crushing action on the material to be extruded and to prevent the latter from slipping out of the pressure area.
- the resulting extruded material is sheared by means of fixed blades operating on the external surface of the extruder to form the pellets.
- EP-A-0371519 discloses a wood pellet machine according to the preamble of claim 1, comprising a treatment chamber, a rotating annular extruder turning in said chamber and provided with a plurality of radial holes, and rotating pressure rollers, positioned and operating at a tangent to the internal surface of the perforated extruder.
- a pressure roller is associated with the extruder and can be positioned radially to the Internal surface of the extruder by means of an oleodynamic actuator fixed to the housing defining the treatment chamber.
- DE 3813081 discloses a wood pellet machine provided with a die, which itself is provided with bores, and a pan grinder head with pan grinder rollers which roll on the die.
- a hydraulic device is connected to a pump for pressing the pan grinder rollers towards the die.
- a volumetric device is provided to control the flowing of the hydraulic fluid thereby permitting the distance between the pan grinder rollers and the die to be measured and controlled or regulated.
- JP 2002283346 discloses a wood pellet machine wherein the temperature of the die and the rollers is measured to feedback control the operation of the machine with respect to the adjustment of the distance between the rollers and the die.
- the object of this invention is to resolve the problems of the pellet machines of the known technique, by providing a simplified and effective design.
- the advantage of the above is that the pellet machine with cylindrical extrusion is simpler, less cumbersome and not as noisy and can be easily adjusted to the pressure of the extrusion of the initial material so as to optimise on the machine operating capacity and productivity.
- the pressure roller can also be set up for axial positioning, which offers the possibility of using an extruder on the same pellet machining with at least two work sessions and usable alternatively, depending on the material to be pelletised, by simply moving the pressure roller from one work section to another.
- FIG. 10 indicates generically the casing of a pellet machine supporting a annular extruder 11, that is cylindrical, at a horizontal axis, to which a pressure roller 12 is actively associated.
- the extruder 11 is supported by two rings or flanges 13 and turns powered preferably by an oleodynamic motor 14. As is known, the extruder 11 is equipped with numerous radial holes - not shown - for extruding the initial material and is housed and operates in a chamber formed by the casing 10 and closed at the front by a door 15.
- the pressure roller 12 is coordinated and interacts with the internal surface of the annular extruder 11 where the material to be pelletised arrives from an external source.
- Said roller has a knurled peripheral surface 16 and is assembled, by the use of a bearing 17, on a relative shaft 18 parallel to the rotation axis of the extruder 11.
- the shaft 18 of the pressure roller 12 is supported by a support 19 integrated with a piston 20 that is housed and slides in a corresponding oleodynamic cylinder 21 fixed to the door 15.
- the piston and relative cylinder are oriented radially to the shaft 18 of the pressure roller 12, and when said roller is associated with the extruder 11 it is inside the extruder itself. Thanks to this type of assembly, the pressure roller 12 can be positioned radially to the internal surface of the extruder, approaching or moving away from it according to needs, simply by means of an external activation command of the oleodynamic cylinder.
- the material to be pelletised is conveyed from the outside to the inside of the extruder, between the surface of the latter and the pressure roller, where an action is developed that pushes the material through the holes of the extruder, extruding it to form pellets.
- the pressure roller 12 with its connected radial oleodynamic positioning system 20, 21 can be assembled on a guided plate parallel to the roller axis and moved by at least one cylinder 22.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Processing And Handling Of Plastics And Other Materials For Molding In General (AREA)
- Dry Formation Of Fiberboard And The Like (AREA)
- Chemical And Physical Treatments For Wood And The Like (AREA)
Description
- This invention concerns vertical, cylindrical extruder pellet machines in general with internal pressure rollers, and refers in particular to an extruder group for such machines.
- The machines taken into consideration here and used for pelletising wood, usually include a rotating annular extruder, having a large number of radial holes and pressing rollers, also turning, positioned and operating at a tangent to the inner surface of the perforated extruder.
- The starting raw material to be made into pellets is forwarded and crushed between the pressure rollers and the inner surface of the extruder and forced, in this way, to be extruded through the holes in the die. The pressure rollers are usually knurled to increase the crushing action on the material to be extruded and to prevent the latter from slipping out of the pressure area. The resulting extruded material is sheared by means of fixed blades operating on the external surface of the extruder to form the pellets.
- In the known pellet machines, the rotation of the extruder is powered by an external motor unit using a belt or pulley drive, which besides being extremely cumbersome is also noisy. Furthermore, there are two or more pressure rollers and adjustment of their position with reference to the extruder is always a problem.
-
EP-A-0371519 discloses a wood pellet machine according to the preamble of claim 1, comprising a treatment chamber, a rotating annular extruder turning in said chamber and provided with a plurality of radial holes, and rotating pressure rollers, positioned and operating at a tangent to the internal surface of the perforated extruder. A pressure roller is associated with the extruder and can be positioned radially to the Internal surface of the extruder by means of an oleodynamic actuator fixed to the housing defining the treatment chamber. -
DE 3813081 discloses a wood pellet machine provided with a die, which itself is provided with bores, and a pan grinder head with pan grinder rollers which roll on the die. A hydraulic device is connected to a pump for pressing the pan grinder rollers towards the die. A volumetric device is provided to control the flowing of the hydraulic fluid thereby permitting the distance between the pan grinder rollers and the die to be measured and controlled or regulated. -
JP 2002283346 -
SU 709386 - The object of this invention is to resolve the problems of the pellet machines of the known technique, by providing a simplified and effective design.
- The advantage of the above is that the pellet machine with cylindrical extrusion is simpler, less cumbersome and not as noisy and can be easily adjusted to the pressure of the extrusion of the initial material so as to optimise on the machine operating capacity and productivity.
- Furthermore, the pressure roller can also be set up for axial positioning, which offers the possibility of using an extruder on the same pellet machining with at least two work sessions and usable alternatively, depending on the material to be pelletised, by simply moving the pressure roller from one work section to another.
- The object and the advantages mentioned above are achieved, in compliance with the invention, using an improved wood pellet machine according to at least claim 1.
- The invention will however become more evident in the continuation of this description made in reference to the enclosed exemplifying drawings, in which:
-
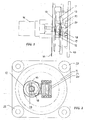
Fig.1 is a schematic lateral view of the extruder group; and -
Fig. 2 is a front view of the extruder-pressure roller connection. - In said
drawing 10 indicates generically the casing of a pellet machine supporting aannular extruder 11, that is cylindrical, at a horizontal axis, to which apressure roller 12 is actively associated. - The
extruder 11 is supported by two rings orflanges 13 and turns powered preferably by anoleodynamic motor 14. As is known, theextruder 11 is equipped with numerous radial holes - not shown - for extruding the initial material and is housed and operates in a chamber formed by thecasing 10 and closed at the front by adoor 15. - The
pressure roller 12 is coordinated and interacts with the internal surface of theannular extruder 11 where the material to be pelletised arrives from an external source. Said roller has a knurledperipheral surface 16 and is assembled, by the use of abearing 17, on arelative shaft 18 parallel to the rotation axis of theextruder 11. - The
shaft 18 of thepressure roller 12 is supported by a support 19 integrated with apiston 20 that is housed and slides in a corresponding oleodynamic cylinder 21 fixed to thedoor 15. The piston and relative cylinder are oriented radially to theshaft 18 of thepressure roller 12, and when said roller is associated with theextruder 11 it is inside the extruder itself. Thanks to this type of assembly, thepressure roller 12 can be positioned radially to the internal surface of the extruder, approaching or moving away from it according to needs, simply by means of an external activation command of the oleodynamic cylinder. - The material to be pelletised is conveyed from the outside to the inside of the extruder, between the surface of the latter and the pressure roller, where an action is developed that pushes the material through the holes of the extruder, extruding it to form pellets.
- In addition, the
pressure roller 12 with its connected radialoleodynamic positioning system 20, 21 can be assembled on a guided plate parallel to the roller axis and moved by at least onecylinder 22. In this way and as stated above, it will be possible to set up an extruder with at least two parallel, side by side, work sections, and use one or the other work section by axially moving the pressure roller from one work section to the other. - Worthy of mention is the fact that the supply of the material to the extruder of the machine is achieved by screw feed driven by a device with auto-adjusted rotating speed by an electronic and oleodynamic retroaction (Load-Sensing) and that the extruder can be associated with an automatic cleaning and lubricating system by an electro-oleodynamic control (Easy-Start).
Claims (5)
- A wood pellet machine, comprising a treatment chamber, a rotating annular extruder (11) turning in said chamber and provided with radial holes, and rotating pressure rollers (12) positioned and operating at a tangent to the internal surface of the perforated extruder (11), wherein said annular extruder (11) is associated with a pressure roller (12) supported by a movable support and which is able to be positioned radially to the internal surface of the extruder (11) by means of an oleodynamic actuator (20, 21), wherein the pressure roller (12) has a shaft (18) parallel to the rotating axis of the extruder (11), and wherein said shaft (18) is supported by a support (19) integrated with a piston (20) housed and sliding in an oleodynamic cylinder (21), characterized in that said oleodynamic cylinder (21) is fixed to a closing door (15) of the treatment chamber, said piston (20) and relative cylinder (21) being radially oriented to the shaft (18) of said pressure roller (12).
- Pellet machine according to claim 1, wherein the extruder (11) has two different work sections placed side by side and wherein said pressure roller (12) is able to be moved and positioned axially in correlation with one or the other of said work sections of the extruder (11).
- Pellet machine according to claim 2, wherein, for its axial positioning, said pressure roller (12) is assembled on a means of support (19) movable by means of at least one oleodynamic cylinder (21).
- Pellet machine according to any of the previous claims, wherein the rotating annular extruder (11) is driven by an oleodynamic motor (14).
- Pellet machine according to any of the previous claims, wherein said pressure roller (12) is associated with said extruder (11) and is able to be moved and positioned both radially and axially to the internal surface of the extruder (11) by means of a remote controlled oleodynamic actuator.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| PL05425162T PL1619012T3 (en) | 2004-07-21 | 2005-03-21 | Pellet machine with oleodynamic control extruder group |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT000086A ITBS20040086A1 (en) | 2004-07-21 | 2004-07-21 | PELLETTING MACHINE WITH HYDRAULIC CONTROL DRAWING UNIT |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1619012A2 EP1619012A2 (en) | 2006-01-25 |
| EP1619012A3 EP1619012A3 (en) | 2008-02-27 |
| EP1619012B1 true EP1619012B1 (en) | 2012-09-05 |
Family
ID=34980095
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP05425162A Expired - Lifetime EP1619012B1 (en) | 2004-07-21 | 2005-03-21 | Pellet machine with oleodynamic control extruder group |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP1619012B1 (en) |
| ES (1) | ES2392435T3 (en) |
| IT (1) | ITBS20040086A1 (en) |
| PL (1) | PL1619012T3 (en) |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| SU709386A1 (en) * | 1977-01-26 | 1980-01-18 | Приморский научно-исследовательский институт сельского хозяйства | Granulating press |
| DE3775423D1 (en) * | 1986-01-24 | 1992-02-06 | Buehler Ag | Wuerfelpresse. |
| DE3813081A1 (en) * | 1988-04-19 | 1989-11-02 | Kahl Amandus Maschf | Pan grinder press with a hydraulic device |
| JP2002283346A (en) * | 2001-03-23 | 2002-10-03 | Nkk Corp | Waste plastic granulator |
-
2004
- 2004-07-21 IT IT000086A patent/ITBS20040086A1/en unknown
-
2005
- 2005-03-21 PL PL05425162T patent/PL1619012T3/en unknown
- 2005-03-21 ES ES05425162T patent/ES2392435T3/en not_active Expired - Lifetime
- 2005-03-21 EP EP05425162A patent/EP1619012B1/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| EP1619012A3 (en) | 2008-02-27 |
| ES2392435T3 (en) | 2012-12-10 |
| EP1619012A2 (en) | 2006-01-25 |
| ITBS20040086A1 (en) | 2004-10-21 |
| PL1619012T3 (en) | 2013-01-31 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US7033152B2 (en) | Underwater pelletizer with positively controlled cutter HUB | |
| US5110523A (en) | Method and apparatus for maintaining a constant contact pressure on elements for cutting under water in granulator machines | |
| CN1187178C (en) | Method and apparatus for making shaped articles | |
| US8544777B2 (en) | Recycling machine for processing reused materials | |
| US20140183796A1 (en) | Extrusion blow molding machine and blow molding method using the machine | |
| CN1048352A (en) | Apparatus for continuous production of laminated plastics | |
| CN102886912B (en) | Rotary plunger biomass molding machine | |
| CA2152564C (en) | Extrusion machine | |
| JP2009066974A (en) | Underwater cutting and granulating method, and underwater cut granulator | |
| JP5485036B2 (en) | Dehydrator | |
| US5587186A (en) | Apparatus for pelletizing plastics | |
| EP1619012A2 (en) | Pellet machine with oleodynamic control extruder group | |
| US5599264A (en) | Roller width adjusting device for a divided type molding roller | |
| CN101402126A (en) | Internal ribbed tube molding device | |
| WO1998017464A1 (en) | Pelletizing press | |
| CN1330478C (en) | Pelleting press | |
| US4556381A (en) | Press for producing pellets from bulk material | |
| WO2010026461A2 (en) | Apparatus for producing pellets | |
| EP3331783B1 (en) | Conveyor pulley and process for producing a roller tube | |
| CN218286601U (en) | Single-cylinder injection device of injection molding machine | |
| US5527176A (en) | Pelletizer | |
| KR20100089440A (en) | Machine for forming pellets | |
| JPH06101945A (en) | Rotating cylinder type processing equipment | |
| JPH05228923A (en) | Granulating method and apparatus for plastics | |
| CN116442584A (en) | Solid waste treatment device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR LV MK YU |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA HR LV MK YU |
|
| 17P | Request for examination filed |
Effective date: 20080620 |
|
| AKX | Designation fees paid |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| 17Q | First examination report despatched |
Effective date: 20111011 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IS IT LI LT LU MC NL PL PT RO SE SI SK TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 573892 Country of ref document: AT Kind code of ref document: T Effective date: 20120915 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602005035975 Country of ref document: DE Effective date: 20121031 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2392435 Country of ref document: ES Kind code of ref document: T3 Effective date: 20121210 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20120402315 Country of ref document: GR Effective date: 20121122 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 |
|
| REG | Reference to a national code |
Ref country code: PL Ref legal event code: T3 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130105 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20130107 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 |
|
| 26N | No opposition filed |
Effective date: 20130606 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20120905 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602005035975 Country of ref document: DE Effective date: 20130606 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130331 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130321 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130331 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130331 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20050321 Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20130321 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20160326 Year of fee payment: 12 Ref country code: LT Payment date: 20160301 Year of fee payment: 12 Ref country code: ES Payment date: 20160328 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 20160302 Year of fee payment: 12 Ref country code: FR Payment date: 20160328 Year of fee payment: 12 Ref country code: GB Payment date: 20160329 Year of fee payment: 12 Ref country code: GR Payment date: 20160329 Year of fee payment: 12 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20160331 Year of fee payment: 12 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602005035975 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MM4D Effective date: 20170321 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170321 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20170401 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MM01 Ref document number: 573892 Country of ref document: AT Kind code of ref document: T Effective date: 20170321 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20170321 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20171130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170321 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171003 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170331 Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170401 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170321 Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20171005 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: RO Payment date: 20180227 Year of fee payment: 14 Ref country code: CZ Payment date: 20180226 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20180216 Year of fee payment: 14 Ref country code: BG Payment date: 20180219 Year of fee payment: 14 Ref country code: PL Payment date: 20180215 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20180705 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20170322 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190321 Ref country code: CZ Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190321 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190930 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190321 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20190321 |