EP0986500B1 - Can with easy open end - Google Patents
Can with easy open end Download PDFInfo
- Publication number
- EP0986500B1 EP0986500B1 EP98921661A EP98921661A EP0986500B1 EP 0986500 B1 EP0986500 B1 EP 0986500B1 EP 98921661 A EP98921661 A EP 98921661A EP 98921661 A EP98921661 A EP 98921661A EP 0986500 B1 EP0986500 B1 EP 0986500B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- score
- grain
- tab
- chord
- arc
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 239000002184 metal Substances 0.000 claims abstract description 14
- 238000006243 chemical reaction Methods 0.000 claims description 8
- 238000005304 joining Methods 0.000 claims description 7
- 238000004519 manufacturing process Methods 0.000 claims description 4
- FGUUSXIOTUKUDN-IBGZPJMESA-N C1(=CC=CC=C1)N1C2=C(NC([C@H](C1)NC=1OC(=NN=1)C1=CC=CC=C1)=O)C=CC=C2 Chemical compound C1(=CC=CC=C1)N1C2=C(NC([C@H](C1)NC=1OC(=NN=1)C1=CC=CC=C1)=O)C=CC=C2 FGUUSXIOTUKUDN-IBGZPJMESA-N 0.000 claims description 2
- 238000005520 cutting process Methods 0.000 claims description 2
- 230000000694 effects Effects 0.000 description 3
- 230000002411 adverse Effects 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 150000001875 compounds Chemical class 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 230000002093 peripheral effect Effects 0.000 description 1
- 230000000644 propagated effect Effects 0.000 description 1
- 238000004826 seaming Methods 0.000 description 1
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D17/00—Rigid or semi-rigid containers specially constructed to be opened by cutting or piercing, or by tearing of frangible members or portions
- B65D17/28—Rigid or semi-rigid containers specially constructed to be opened by cutting or piercing, or by tearing of frangible members or portions at lines or points of weakness
- B65D17/401—Rigid or semi-rigid containers specially constructed to be opened by cutting or piercing, or by tearing of frangible members or portions at lines or points of weakness characterised by having the line of weakness provided in an end wall
- B65D17/4011—Rigid or semi-rigid containers specially constructed to be opened by cutting or piercing, or by tearing of frangible members or portions at lines or points of weakness characterised by having the line of weakness provided in an end wall for opening completely by means of a tearing tab
Definitions
- This invention relates to an easy open end and, in particular, to a metal can end of the so-called “full aperture” type, having a circumferential score which enables a circular panel of the end to be removed for access to a product within the can.
- An easy open can end having a full aperture easy opening feature typically comprises a seaming panel, a chuck wall and a countersink joining the chuck wall to a central panel.
- a circumferential score is provided adjacent the countersink and a metal tab is riveted to the central panel so that its nose is positioned above the score.
- the nose of the metal tab pierces the score directly when the handle is lifted. Breaking the score takes place in three stages. Firstly, by lifting the handle, the score tears or "pops" and an initial arc is severed as the tab is lifted to the position where the tab is perpendicular to the end. By pushing the tab over in a second action until it meets the peripheral chuck wall of the end, the initial score tear is propagated. In the third stage, the tab and end panel are pulled out away from the can body so that the end peels away from the can body.
- the tear force required to remove the central panel in the final stage is reduced.
- the maximum chord length achievable may be dictated by various factors, including the maximum tilting of the tab to meet the chuck wall.
- the force required for the first stage of opening i.e. the "pop" force, may exceed acceptable values.
- the present invention seeks to reduce tear force requirements by achieving a large chord length without adversely affecting the pop force requirements.
- a metal can end comprising a central panel; a circumferential score; and a tab fixed to the central panel adjacent the score with its longitudinal axis along a radius of the end such that, when the tab is raised, an arc of the score is broken, the arc having a chord joining its ends; characterised in that the grain of the metal end has an angle which is ⁇ 15° to 60° to the longitudinal axis of the tab.
- a metal can end comprising a centre panel, a circumferential score and a tab fixed to the panel adjacent the score such that, when the tab is raised, an arc of the score is broken, the arc having a chord joining its ends; characterised in that the metal of the can end has a grain which is parallel to a tangent to the can end in the same plane as the can end and at one end of the chord.
- the grain is between +/- 10° to the tangent to the can end at one end of the chord.
- the score may have a residual which is lower at the end of the chord having the tangent to which the grain is aligned than at the other.
- a method of making a can end such as is described above, the method comprising a) cutting blanks from a metal sheet; b) forming the blanks into end shells; c) lining the shells; d) feeding the shells into a conversion press; e) forming a score (10); and f) fixing a tab to the shell; characterised by, between steps d) and e): determining the orientation of each shell; lifting each shell and turning it until the shell has its grain substantially parallel to a predetermined tangential position; and characterised in that step f) is carried out such that the longitudinal axis of the tab is ⁇ 15° to 60° to the grain.
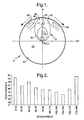
- FIG. 1 shows a full aperture easy open end 5 having a circumferential score 10.
- the end is openable by means of a tab 15 fixed to a central panel 20 of the end, along a radius thereof.
- the tab 15 is fixed to the central panel 20 by means of a rivet 25 and has a ring pull handle 30 at one end and a nose 35 at its opposite end, adjacent the score 10.
- the handle 30 In order to open the can end, the handle 30 is first raised and the tab pivots about the rivet 25 in order to "pop" the score 10. This action causes the central panel 20 to fold along a chord 40 as the score is broken along arc 45. Complete opening of the end is achieved by pulling along the radius in the direction of the large arrow 50, thereby removing the whole of the central panel 20.
- the tear force was measured with the grain at varying angles around the can end.
- the "grain angle” is defined as the angle between the radius of the end along which the user pulls the tab (i.e. the direction of arrow 50) and the grain direction, measured in the clockwise direction from arrow 50.
- the effect of the grain angle on tear force is shown in figure 2.
- the tear force would be least, in fact these angles yielded the highest tear force readings.
- the lowest tear force was found at 135° to 150°. It is believed that since the central panel 20 folds along chord 40 in order to pop the score, in practice the tear force can be said to have a component along tangents at the ends of this chord, in the plane of the end. This explains the low reading at 135° to 150° since in theory lowest tear forces should' then occur when the tangents are at ⁇ 45° (45° and 135°) to the pulling action, arrow 50. However, this did not explain why the tear force was high in the grain angle range of 35° to 50°.
- figure 2 show an unexpectedly high tear force in the 35° to 50° range, but this is also higher than the tear forces in the adjacent ranges, 15° to 30° and 55° to 70°.
- This variation may be due to the length of chord 40 since tangents 55 and 60 at the ends of the chord are not necessarily at precisely ⁇ 45°. It should be remembered, however, that even if one of the tangents is aligned with the grain, i.e. parallel to the grain, which results in a lower tear force component along that tangent, the tear force component along the tangent at the opposite end of the chord may not be particularly low and the tear force is the sum of these components.
- the Applicant has surprisingly found a further factor which influences tear force. After popping the score, different score depths were measured at the ends of the chord 40. At a grain angle of 45°, the score residual was 127 ⁇ m whereas the residual at 135° was 119 ⁇ m. This explains why the tear force is lowest at 135° since the grain angle coincides with minimum score residual at that angle.
- tear force component is across the grain at minimum score residual, it is not necessarily less than the other component which may be along the grain and at a higher score residual. Ideally, therefore, it appears that the grain should be aligned to the tangent at the end of the score having minimum score residual.
- the score (i.e. the score residual thickness) is measured in table 1 at the 1 o'clock, "score 1", and 11 o'clock, “score 11" positions. From the table it is clear that the values for score 11 are always significantly greater than those of score 1, the average difference being 8 microns greater.
- the end of the present invention is manufactured using conventional shell manufacturing steps, where a shell is first pressed and any lining compound inserted, after which the shell is indexed into the conversion press for score, rivet and tab to be added.
- a camera is used to check grain orientation as the shell is indexed into the conversion press and a lifter and servomotor driven turntable orient the end to the desired grain angle. Modifications to the conversion press ensure that score residual is minimum when the grain is oriented to the expected chord tangent. This tangent varies according to the end diameter, typically being in the following quadrants: Diameter (mm) Degrees 65 30 - 50 73 24 - 45 84 20 - 40 99 18 - 38
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Containers Opened By Tearing Frangible Portions (AREA)
- Control And Other Processes For Unpacking Of Materials (AREA)
- Dental Tools And Instruments Or Auxiliary Dental Instruments (AREA)
- Closures For Containers (AREA)
- Undergarments, Swaddling Clothes, Handkerchiefs Or Underwear Materials (AREA)
- Food-Manufacturing Devices (AREA)
Abstract
Description
| Diameter (mm) | Degrees |
| 65 | 30 - 50 |
| 73 | 24 - 45 |
| 84 | 20 - 40 |
| 99 | 18 - 38 |
| Score 1 (microns) | Score 11 (microns) | Difference (microns) | |
| 120 | 126 | 5.91 | |
| 120 | 126 | 5.91 | |
| 118 | 128 | 9.84 | |
| 118 | 128 | 9.84 | |
| 120 | 128 | 7.87 | |
| 122 | 128 | 5.91 | |
| 122 | 128 | 5.91 | |
| 120 | 128 | 7.87 | |
| 122 | 128 | 5.91 | |
| 118 | 126 | 7.87 | |
| 120 | 128 | 7.87 | |
| 120 | 130 | 9.84 | |
| 120 | 130 | 9.84 | |
| 118 | 132 | 13.78 | |
| 120 | 132 | 11.81 | |
| 122 | 134 | 11.81 | |
| 124 | 130 | 5.91 | |
| 126 | 130 | 3.94 | |
| 124 | 128 | 3.94 | |
| 120 | 128 | 7.87 | |
| Averages: | 121 | 129 | 8 |
Claims (8)
- A metal can end (5) comprising a central panel (20); a circumferential score (10); and a tab (15) fixed to the central panel (20) adjacent the score (10) with its longitudinal axis along a radius of the end such that, when the tab is raised, an arc (45) of the score is broken, the arc (45) having a chord (40) joining its ends;
characterised in that the grain of the metal end has an angle which is ± 15° to 60° to the longitudinal axis of the tab. - An end according to claim 1, in which the end has a diameter of 80 to 100 mm and the grain angle is 15° to 45°.
- An end according to claim 1, in which the end has a diameter of 60 to 80 mm and the grain angle is 20° to 60°.
- An end according to any one of claims 1 to 3, in which a tangent in the plane of the end and at one end of the chord to the arc which is fomed when the tab is raised, is parallel to the grain of the end.
- A metal can end (5) comprising a centre panel (20), a circumferential score (10) and a tab (15) fixed to the panel (20) adjacent the score (10) such that, when the tab is raised, an arc (45) of the score is broken, the arc having a chord (40) joining its ends;
characterised in that the metal of the can end has a grain which is parallel to a tangent to the can end in the same plane as the can end and at one end of the chord (40). - An end according to claim 4 or claim 5, in which the grain is between +/- 10° to the tangent.
- An end according to any one of claims 4 to 6, in which the score has a residual which is lower at the end of the chord having the tangent to which the grain is aligned than at the other.
- A method of making a can end (5) according to any one of claims 1 to 7, comprising:characterised by, between steps d) and e):a) cutting blanks from a metal sheet;b) forming the blanks into end shells;c) lining the shells;d) feeding the shells into a conversion press;e) forming a score (10); andf) fixing a tab (15) to the shell;characterised in that step f) is carried out such that the longitudinal axis of the tab is ± 15° to 60° to the grain.determining the orientation of each shell;lifting each shell and turning it until the shell has its grain substantially parallel to a predetermined tangential position; and
Applications Claiming Priority (3)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| GB9711290 | 1997-06-03 | ||
| GBGB9711290.8A GB9711290D0 (en) | 1997-06-03 | 1997-06-03 | Easy open ends |
| PCT/GB1998/001448 WO1998055366A1 (en) | 1997-06-03 | 1998-05-19 | Can with easy open end |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0986500A1 EP0986500A1 (en) | 2000-03-22 |
| EP0986500B1 true EP0986500B1 (en) | 2002-08-14 |
Family
ID=10813382
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP98921661A Expired - Lifetime EP0986500B1 (en) | 1997-06-03 | 1998-05-19 | Can with easy open end |
Country Status (9)
| Country | Link |
|---|---|
| US (1) | US6341709B1 (en) |
| EP (1) | EP0986500B1 (en) |
| AT (1) | ATE222200T1 (en) |
| AU (1) | AU7444198A (en) |
| CA (1) | CA2292649C (en) |
| DE (1) | DE69807218T2 (en) |
| ES (1) | ES2182304T3 (en) |
| GB (1) | GB9711290D0 (en) |
| WO (1) | WO1998055366A1 (en) |
Families Citing this family (64)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP1052039A1 (en) * | 1999-05-12 | 2000-11-15 | Showa Seiki Co., Ltd. | Can lid and method of manufacturing same |
| JP4428797B2 (en) * | 1999-05-18 | 2010-03-10 | 昭和製器株式会社 | Can lid manufacturing equipment |
| EP1308226A1 (en) * | 2001-11-06 | 2003-05-07 | Impress B.V. | Easy opening closure, container provided with such closure, and apparatus for producing such closure |
| ES2238116B1 (en) * | 2002-11-07 | 2006-12-01 | Mivisa Envases, S.A.U. | EASY OPEN COVER. |
| USD653124S1 (en) | 2007-12-17 | 2012-01-31 | Silgan Containers Llc | Container |
| USD588019S1 (en) | 2007-12-17 | 2009-03-10 | Silgan Containers Corporation | Container |
| USD588018S1 (en) | 2008-02-27 | 2009-03-10 | Silgan Containers Corporation | Container |
| US20090218349A1 (en) * | 2008-02-29 | 2009-09-03 | Silgan Containers Corporation | Vacuum container with protective features |
| USD672663S1 (en) | 2008-02-27 | 2012-12-18 | Silgan Containers Llc | Container |
| USD652740S1 (en) | 2008-02-27 | 2012-01-24 | Silgan Containers Llc | Container |
| US8141741B2 (en) * | 2008-02-27 | 2012-03-27 | Silgan Containers Llc | Vacuum container with protective features |
| USD632189S1 (en) | 2008-03-28 | 2011-02-08 | Silgan Containers Llc | Container |
| USD614970S1 (en) | 2008-03-28 | 2010-05-04 | Silgan Containers Llc | Container |
| USD596958S1 (en) | 2008-03-28 | 2009-07-28 | Silgan Containers Corporation | Container |
| USD626015S1 (en) | 2008-03-28 | 2010-10-26 | Silgan Containers Llc | Container |
| USD641261S1 (en) | 2008-03-28 | 2011-07-12 | Silgan Containers, Llc | Container |
| USD596505S1 (en) | 2008-03-28 | 2009-07-21 | Silgan Containers Corporation | Container |
| USD632188S1 (en) | 2008-03-28 | 2011-02-08 | Silgan Containers Llc | Container |
| USD596502S1 (en) | 2008-03-28 | 2009-07-21 | Silgan Containers Corporation | Container |
| USD596955S1 (en) | 2008-03-28 | 2009-07-28 | Silgan Containers Corporation | Container |
| USD596500S1 (en) | 2008-03-28 | 2009-07-21 | Silgan Containers Corporation | Container |
| USD632187S1 (en) | 2008-03-28 | 2011-02-08 | Silgan Containers Llc | Container |
| USD632190S1 (en) | 2008-03-28 | 2011-02-08 | Silgan Containers Llc | Container |
| USD596501S1 (en) | 2008-03-28 | 2009-07-21 | Silgan Containers Corporation | Container |
| USD596956S1 (en) | 2008-03-28 | 2009-07-28 | Silgan Containers Corporation | Container |
| USD588016S1 (en) | 2008-04-04 | 2009-03-10 | Silgan Containers Corporation | Container |
| USD653562S1 (en) | 2008-04-04 | 2012-02-07 | Silgan Containers Llc | Container |
| USD652741S1 (en) | 2008-04-04 | 2012-01-24 | Silgan Containers Llc | Container |
| USD588020S1 (en) | 2008-04-04 | 2009-03-10 | Silgan Containers Corporation | Container |
| USD588017S1 (en) | 2008-04-04 | 2009-03-10 | Silgan Containers Corporation | Container |
| USD588021S1 (en) | 2008-04-04 | 2009-03-10 | Silgan Containers Corporation | Container |
| USD653563S1 (en) | 2008-04-04 | 2012-02-07 | Silgan Containers Llc | Container |
| USD653123S1 (en) | 2008-04-04 | 2012-01-31 | Silgan Containers Llc | Container |
| USD606403S1 (en) | 2008-05-12 | 2009-12-22 | Silgan Containers Llc | Container |
| USD612732S1 (en) | 2008-05-12 | 2010-03-30 | Silgan Containers Llc | Container |
| USD614969S1 (en) | 2008-05-12 | 2010-05-04 | Silgan Containers Llc | Container |
| USD607727S1 (en) | 2008-05-12 | 2010-01-12 | Silgan Containers Llc | Container |
| USD596957S1 (en) | 2008-05-12 | 2009-07-28 | Silgan Containers Corporation | Container |
| USD620377S1 (en) | 2008-05-12 | 2010-07-27 | Silgan Containers Llc | Container |
| USD649887S1 (en) | 2008-05-12 | 2011-12-06 | Silgan Containers Llc | Container |
| USD624438S1 (en) | 2008-05-12 | 2010-09-28 | Silgan Containers, Llc | Container |
| USD607330S1 (en) | 2008-05-12 | 2010-01-05 | Silgan Containers Llc | Container |
| USD606406S1 (en) | 2008-05-12 | 2009-12-22 | Silgan Containers Llc | Container |
| USD652742S1 (en) | 2008-05-12 | 2012-01-24 | Silgan Containers Llc | Container |
| USD638311S1 (en) | 2008-05-12 | 2011-05-24 | Silgan Containers, Llc | Container |
| USD606405S1 (en) | 2008-05-12 | 2009-12-22 | Silgan Containers Llc | Container |
| USD606402S1 (en) | 2008-05-12 | 2009-12-22 | Silgan Containers Llc | Container |
| USD596503S1 (en) | 2008-05-12 | 2009-07-21 | Silgan Containers Corporation | Container |
| USD606404S1 (en) | 2008-05-12 | 2009-12-22 | Silgan Containers Llc | Container |
| USD607329S1 (en) | 2008-05-12 | 2010-01-05 | Silgan Containers Llc | Container |
| USD596504S1 (en) | 2008-05-12 | 2009-07-21 | Silgan Containers Corporation | Container |
| US8701887B2 (en) | 2008-07-31 | 2014-04-22 | Silgan Containers Llc | Stackable container |
| USD615877S1 (en) | 2009-02-05 | 2010-05-18 | Silgan Containers Llc | Container |
| USD651527S1 (en) | 2009-02-05 | 2012-01-03 | Silgan Containers Llc | Container |
| USD614049S1 (en) | 2009-03-02 | 2010-04-20 | Silgan Containers Llc | Container |
| USD631759S1 (en) | 2009-03-02 | 2011-02-01 | Silgan Containers Llc | Container |
| USD653125S1 (en) | 2009-09-09 | 2012-01-31 | Silgan Containers Llc | Container |
| USD653126S1 (en) | 2009-09-30 | 2012-01-31 | Silgan Containers Llc | Container |
| USD651526S1 (en) | 2009-12-29 | 2012-01-03 | Silgan Containers Llc | Container |
| USD658078S1 (en) | 2010-04-30 | 2012-04-24 | Silgan Containers Llc | Container |
| USD656042S1 (en) | 2010-10-01 | 2012-03-20 | Silgan Containers Llc | Container |
| DE102011075211A1 (en) | 2011-05-04 | 2012-11-08 | C2C Beteiligungs-Gmbh | Lid arrangement for a container and a container with such a lid arrangement |
| US9333289B1 (en) | 2015-01-16 | 2016-05-10 | Plas-Tech Engineering, Inc. | Tamper evident closure container |
| WO2017123502A1 (en) * | 2016-01-13 | 2017-07-20 | Ball Corporation | System and method for orienting the rolling direction of an end shell in a metal container manufacturing process |
Family Cites Families (12)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3628650A (en) * | 1969-11-14 | 1971-12-21 | American Can Co | Apparatus for orienting can ends |
| US3799390A (en) * | 1971-12-21 | 1974-03-26 | Reynolds Metals Co | Easy open end closure |
| US3902626A (en) * | 1974-06-06 | 1975-09-02 | Aluminum Co Of America | Easy opening container component |
| US4015744A (en) * | 1975-10-28 | 1977-04-05 | Ermal C. Fraze | Easy-open ecology end |
| US4073399A (en) * | 1976-02-25 | 1978-02-14 | Aluminum Company Of America | Tear-off closure |
| GB1574226A (en) * | 1976-06-14 | 1980-09-03 | Styner & Bienz Ag | Method of producing a cover for a tin having a weakening scoring for tearing it open apparatus for carrying out this method and a cover produced in accordance with such method |
| US4024981A (en) * | 1976-07-01 | 1977-05-24 | Ermal C. Fraze | Easy-open ecology end |
| US4862722A (en) * | 1984-01-16 | 1989-09-05 | Dayton Reliable Tool & Mfg. Co. | Method for forming a shell for a can type container |
| NZ210588A (en) * | 1984-01-16 | 1988-01-08 | Dayton Reliable Tool & Mfg Co | Shell used in manufacture of can ends: non-circular blank having rounded corners is cut from sheet metal |
| IT1228227B (en) * | 1989-01-12 | 1991-06-05 | Quaker Chiari & Forti S P A P | EASY OPENING CLOSURE FOR METAL SHEET COVERS OF CANS AND SIMILAR. |
| FR2687372B1 (en) * | 1992-02-19 | 1995-05-19 | Lorraine Laminage | EASY OPENING COVER AND CONTAINER PROVIDED WITH SUCH A COVER. |
| US5715964A (en) * | 1996-02-23 | 1998-02-10 | American National Can Company | Can end with emboss and deboss score panel stiffening beads |
-
1997
- 1997-06-03 GB GBGB9711290.8A patent/GB9711290D0/en not_active Ceased
-
1998
- 1998-05-19 EP EP98921661A patent/EP0986500B1/en not_active Expired - Lifetime
- 1998-05-19 AU AU74441/98A patent/AU7444198A/en not_active Abandoned
- 1998-05-19 ES ES98921661T patent/ES2182304T3/en not_active Expired - Lifetime
- 1998-05-19 US US09/424,791 patent/US6341709B1/en not_active Expired - Fee Related
- 1998-05-19 AT AT98921661T patent/ATE222200T1/en not_active IP Right Cessation
- 1998-05-19 CA CA002292649A patent/CA2292649C/en not_active Expired - Fee Related
- 1998-05-19 WO PCT/GB1998/001448 patent/WO1998055366A1/en not_active Ceased
- 1998-05-19 DE DE69807218T patent/DE69807218T2/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| GB9711290D0 (en) | 1997-07-30 |
| EP0986500A1 (en) | 2000-03-22 |
| CA2292649C (en) | 2006-04-04 |
| DE69807218T2 (en) | 2002-12-19 |
| AU7444198A (en) | 1998-12-21 |
| ES2182304T3 (en) | 2003-03-01 |
| ATE222200T1 (en) | 2002-08-15 |
| DE69807218D1 (en) | 2002-09-19 |
| US6341709B1 (en) | 2002-01-29 |
| WO1998055366A1 (en) | 1998-12-10 |
| CA2292649A1 (en) | 1998-12-10 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CA2292649C (en) | Can with easy open end | |
| US4465204A (en) | Pull tab for easy open end | |
| US4804106A (en) | Measures to control opening of full-panel safety-edge, convenience-feature end closures | |
| US4530631A (en) | Pull tab for easy open can end-method of manufacture thereof | |
| AU2002347836B2 (en) | Reformed can end and method therefore | |
| EP1857370A2 (en) | Can End for a Container | |
| EP1514803A2 (en) | Safe opening can end and method of manufacturing | |
| EP2081709B1 (en) | Easy open can end with high pressure venting | |
| AU2005245413B2 (en) | Can end with tab for improved accessibility | |
| US6772900B2 (en) | Can end | |
| JP2010530835A (en) | Can end and method for manufacturing the can end | |
| US3939787A (en) | Convenience closure with safe edges | |
| EP3549881A1 (en) | Can end produced from downgauged blank | |
| US3715051A (en) | Easy opening container | |
| US3986633A (en) | Tab for easy-opening container wall | |
| US3715052A (en) | Full panel self-opening end closure | |
| EP0993347B1 (en) | Tab manufacture | |
| US20080066290A1 (en) | Tooling for making easy open can end | |
| EP1474338B1 (en) | Can end | |
| CN108473230A (en) | Lid for beverage can | |
| US20080069667A1 (en) | Tool for making easy open can end with high pressure venting | |
| US7673490B2 (en) | Method of making an easy open can end with high pressure venting | |
| JPH05502208A (en) | Convenient feature non-circular end closure with interrupted panel contour | |
| AU2000240466A1 (en) | Container end closure edge reforming | |
| JPS6351A (en) | Method of forming cleavage guide line in vessel cover |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19991122 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI NL PT SE |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| 17Q | First examination report despatched |
Effective date: 20011205 |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FI FR GB GR IE IT LI NL PT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020814 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020814 Ref country code: CH Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020814 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20020814 |
|
| REF | Corresponds to: |
Ref document number: 222200 Country of ref document: AT Date of ref document: 20020815 Kind code of ref document: T |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 69807218 Country of ref document: DE Date of ref document: 20020919 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021114 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021114 |
|
| ET | Fr: translation filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20021129 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20020403706 Country of ref document: GR |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2182304 Country of ref document: ES Kind code of ref document: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20030515 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IE Payment date: 20110520 Year of fee payment: 14 Ref country code: GR Payment date: 20110520 Year of fee payment: 14 Ref country code: FR Payment date: 20110607 Year of fee payment: 14 Ref country code: ES Payment date: 20110516 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20110520 Year of fee payment: 14 Ref country code: GB Payment date: 20110520 Year of fee payment: 14 Ref country code: BE Payment date: 20110511 Year of fee payment: 14 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20110520 Year of fee payment: 14 Ref country code: IT Payment date: 20110528 Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R082 Ref document number: 69807218 Country of ref document: DE Representative=s name: RAINER CALLIES, DE Ref country code: DE Ref legal event code: R082 Ref document number: 69807218 Country of ref document: DE Representative=s name: CALLIES, RAINER, DIPL.-PHYS. DR.RER.NAT., DE |
|
| BERE | Be: lapsed |
Owner name: *CROWN CORK & SEAL TECHNOLOGIES CORP. Effective date: 20120531 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: V1 Effective date: 20121201 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20120519 |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: ML Ref document number: 20020403706 Country of ref document: GR Effective date: 20121204 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120531 Ref country code: GR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121204 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120519 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST Effective date: 20130131 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 69807218 Country of ref document: DE Effective date: 20121201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121201 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120531 Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120519 Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120519 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20121201 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20130820 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20120520 |