EP0706940B1 - A method of filling a valve bag and valve bag - Google Patents
A method of filling a valve bag and valve bag Download PDFInfo
- Publication number
- EP0706940B1 EP0706940B1 EP95850175A EP95850175A EP0706940B1 EP 0706940 B1 EP0706940 B1 EP 0706940B1 EP 95850175 A EP95850175 A EP 95850175A EP 95850175 A EP95850175 A EP 95850175A EP 0706940 B1 EP0706940 B1 EP 0706940B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- bag
- valve
- filling
- sheet
- ventilating
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000000034 method Methods 0.000 title claims description 9
- 238000001914 filtration Methods 0.000 claims description 26
- 239000000463 material Substances 0.000 claims description 17
- 238000007789 sealing Methods 0.000 claims description 9
- 239000000428 dust Substances 0.000 claims description 3
- 239000013056 hazardous product Substances 0.000 claims description 2
- 239000004033 plastic Substances 0.000 claims description 2
- 239000003566 sealing material Substances 0.000 claims description 2
- 238000002347 injection Methods 0.000 claims 1
- 239000007924 injection Substances 0.000 claims 1
- 239000003292 glue Substances 0.000 description 7
- 238000004026 adhesive bonding Methods 0.000 description 3
- 230000000694 effects Effects 0.000 description 3
- 239000003795 chemical substances by application Substances 0.000 description 1
- 238000002474 experimental method Methods 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 239000000383 hazardous chemical Substances 0.000 description 1
- 239000012943 hotmelt Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000004745 nonwoven fabric Substances 0.000 description 1
- 238000009423 ventilation Methods 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D31/00—Bags or like containers made of paper and having structural provision for thickness of contents
- B65D31/14—Valve bags, i.e. with valves for filling
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B1/00—Packaging fluent solid material, e.g. powders, granular or loose fibrous material, loose masses of small articles, in individual containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, or jars
- B65B1/04—Methods of, or means for, filling the material into the containers or receptacles
- B65B1/18—Methods of, or means for, filling the material into the containers or receptacles for filling valve-bags
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D33/00—Details of, or accessories for, sacks or bags
- B65D33/01—Ventilation or drainage of bags
Definitions
- the present invention relates to the filling of a valve bag with dust-producing and/or hazardous material, and a valve bag, preferably of the so-called canister type, which is particularly suitable for such use.
- Valve bags are generally used for the transport of various materials. When dust-producing and/or hazardous materials are involved, it is essential that there be no leakage of material to the surroundings when filling the bag with the material and in the subsequent handling. This results in problems especially in the filling operation, when large amounts of air pass into a bag together with the material at issue. The excess pressure arising in the bag involves great risks of leakage to the surroundings and prevents the filling operation from occurring at the desired speed.
- DE-A-41 40 213 discloses a valve bag comprising a filler valve in one corner of one end of the bag and a ventilating valve in the other corner of said one end.
- the object of the present invention is to provide a new filling method and a valve bag which is especially suited for this, thereby alleviating the above-mentioned problems to a considerable degree.
- the invention is thus based on the knowledge that emission of material from the bag to the surroundings - during and after filling - can be kept under extreme control while the filling operation can be carried out in a highly efficient manner by using a tight or non-perforated bag fitted with a special filtering ventilating valve in the bag corner opposite the normal corner-mounted filling valve of the bag, said filling valve being sealed immediately after the filling operation.
- Final evacuation of air, for instance by conventional mangling of the filled bag is advantageously carried out after said sealing of the filling valve, thereby preventing emission of material through the filling valve both in connection with the ending of the filling operation and during the subsequent handling of the bag.
- the filling valve can be sealed in various ways, for instance by means of an externally applied sealing strip or, which at present seems to be preferred, by means arranged inside the filling valve, the sealing effect of these means being achieved by applying, for instance, heat and/or pressure.
- the ventilating valve according to the invention advantageously is a valve fitted with a filtering valve sheet which is transversely folded, its fold facing outwards from the interior of the bag.
- a filtering valve sheet can be very easily mounted in substantially the same manner as a filling valve sheet (which is longitudinally folded) in a conventional so-called valve assembly in a bag-making machine.
- the filtering valve sheet may advantageously be made of crepe filtering paper, although also non-woven fabric could be used.
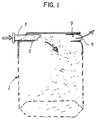
- Fig. 1 schematically illustrates the filling of a bag 1 according to the present invention.
- a filling nozzle 3 is inserted into the filling valve 5 of the bag in one upper corner of the bag.
- Material is injected under pressure through the filling pipe 3, also air being entrained and generating an excess pressure in the bag, which is here assumed to be completely tight, except for a ventilating valve 7 arranged in the other upper corner of the bag and consisting of a filtering sheet of paper 9 attached by gluing.
- the ventilating valve is opened or expanded by the excess pressure so as to expose a large filtering surface, by the filtering sheet being given U-shape (in section), and air leaves through the base of the U, said base being non-glued and therefore being able to provide a large evacuation area.
- the end of the filling pipe 3 is bent to impart to the injected material a direction obliquely downwards in the bag, i.e. away from the ventilating valve. It has surprisingly been found that a ventilating valve according to the invention does not tend to be quickly filled or clogged by injected material, but, on the contrary, yield efficient evacuation of air during the entire filling operation. No active sucking-out of air is necessary.
- the filing pipe 3 can be pulled out of the filling valve 5 which can be immediately sealed, for instance by means of transversely applied bands of selectively activatable sealing material, advantageously of the hot-melt type. Then, a direct, active, terminating continued evacuation of air from the bag may take place through the ventilating air, preferably by mangling of the bag.
- Figs 2 and 3 illustrate an example how to modify according to the present invention a conventional valve bag of the canister type. Since valve bags of this type are well-known, merely modifications which are important to the invention will be discussed in more detail.
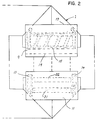
- Fig. 2 illustrates how an unfolded filling valve sheet 11 and a transversely folded filtering valve sheet 9 are glued on each side of the bag to the underlying flat-folded bag side flaps.
- the glue layers of the filling valve sheet 11 are indicated at 13, 14, and the glue layers of the lower part of the filtering valve sheet 9 are indicated at 15.
- the filtering valve sheet 9 has its transverse fold 17 on the outwardly facing side of the sheet.
- the glue layer 15 begins at a considerable distance from the fold 17, such that a comparatively large non-glued area of the lower part of the sheet connects with the fold 17. This also applies to the upper part of the sheet 9, see Fig. 3.
- the lower part of the filtering sheet 9 extends into the bag a shorter distance than does the upper part of the sheet.
- the inner edge of the lower part is indicated at 19.
- the innermost edge area of the lower part advantageously extends beyond the underlying side flap. Especially if this is not possible in view of the width of the bag, a corresponding recess can be formed in the side flap, thereby ensuring free exposure of the innermost edge area of the lower part of the filtering sheet 9.
- Fig. 2 schematically shows also the arrangement of additional, transverse, selectively heat-activatable sealing agent bands 21, 22 on the underside of the filling valve sheet 11, i.e. inside the filling valve itself.
- Fig. 3 shows how the bottom gluing can be carried out. It is apparent that the bottom glue layer 23 can basically be the same for the filling valve sheet 11 and the filtering valve sheet 9, although additional transverse glue bands 25, 26 are arranged for the inner part of the filtering sheet upper part, such that this is safely glued to the bottom of the bag and thus follows this, whereby the U-shaped opening (see Fig. 1) of the ventilating valve will be facilitated.
- the upper part of the filtering sheet 9 has a comparatively large non-glued area connecting with the transverse fold 17.
- the non-glued areas on both sides of the transverse fold 17 permit a large evacuation area to be formed, when the ventilating valve is opened from the inside into U-shape.
- a bottom cover sheet (not shown) glued farthest out should either not cover the above-mentioned non-glued area or, non-glued, cover the same.
- the bag is made of a tight or non-perforated material.
- the invention thus makes it possible to use tight plastic bags, while maintaining the ventilating effect during filling.
- a more efficient evacuation of air and no perforations may permit the use of thinner bag materials.
- non-perforated bags generally leads to reduced emission while emptying the bags and handling the emptied bags.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Bag Frames (AREA)
Description
- The present invention relates to the filling of a valve bag with dust-producing and/or hazardous material, and a valve bag, preferably of the so-called canister type, which is particularly suitable for such use.
- Valve bags are generally used for the transport of various materials. When dust-producing and/or hazardous materials are involved, it is essential that there be no leakage of material to the surroundings when filling the bag with the material and in the subsequent handling. This results in problems especially in the filling operation, when large amounts of air pass into a bag together with the material at issue. The excess pressure arising in the bag involves great risks of leakage to the surroundings and prevents the filling operation from occurring at the desired speed.
- Various forms of evacuation of air from the bags in connection with the filling operation have been suggested. It is common practice to use suitably perforated bags, which involves a risk of leakage. Besides, the evacuation of air will in many cases be unsatisfactory. Experiments have been made with special ventilating means in or in connection with the bag, but in most cases these have been found not to give the desired result.
- DE-A-41 40 213 discloses a valve bag comprising a filler valve in one corner of one end of the bag and a ventilating valve in the other corner of said one end.
- The object of the present invention is to provide a new filling method and a valve bag which is especially suited for this, thereby alleviating the above-mentioned problems to a considerable degree.
- The above-mentioned object is achieved by a method and a valve bag having the features recited in the accompanying claims.
- The invention is thus based on the knowledge that emission of material from the bag to the surroundings - during and after filling - can be kept under extreme control while the filling operation can be carried out in a highly efficient manner by using a tight or non-perforated bag fitted with a special filtering ventilating valve in the bag corner opposite the normal corner-mounted filling valve of the bag, said filling valve being sealed immediately after the filling operation. Final evacuation of air, for instance by conventional mangling of the filled bag, is advantageously carried out after said sealing of the filling valve, thereby preventing emission of material through the filling valve both in connection with the ending of the filling operation and during the subsequent handling of the bag.
- As will be immediately realised by those skilled in the art, the filling valve can be sealed in various ways, for instance by means of an externally applied sealing strip or, which at present seems to be preferred, by means arranged inside the filling valve, the sealing effect of these means being achieved by applying, for instance, heat and/or pressure.
- To ensure the desired ventilation effect, the ventilating valve according to the invention advantageously is a valve fitted with a filtering valve sheet which is transversely folded, its fold facing outwards from the interior of the bag. Such a filtering valve sheet can be very easily mounted in substantially the same manner as a filling valve sheet (which is longitudinally folded) in a conventional so-called valve assembly in a bag-making machine. The filtering valve sheet may advantageously be made of crepe filtering paper, although also non-woven fabric could be used.
- Use of the invention has been found to yield improved evacuation of air and, thus, more efficient filling while reducing the emission problems to a considerable extent.
- The invention will now be described in more detail by way of an embodiment, reference being made to the accompanying drawings.
-
- Fig. 1 is a schematic view, partly in section, which illustrates an example of filling a bag according to the present invention.
- Fig. 2 is a top plan view of the bottom part of an embodiment of a canister-type bag according to the invention, illustrating the position of the transversely folded filtering valve sheet and the filling valve sheet not yet folded, and the associated underlying glue layers.
- Fig. 3 is a view similar to Fig. 2 and illustrates the applied bottom glue layers before the terminating bottom folding and the application and gluing of a bottom cover sheet (not shown).
-
- Fig. 1 schematically illustrates the filling of a
bag 1 according to the present invention. A fillingnozzle 3 is inserted into the fillingvalve 5 of the bag in one upper corner of the bag. Material is injected under pressure through thefilling pipe 3, also air being entrained and generating an excess pressure in the bag, which is here assumed to be completely tight, except for a ventilatingvalve 7 arranged in the other upper corner of the bag and consisting of a filtering sheet ofpaper 9 attached by gluing. The ventilating valve is opened or expanded by the excess pressure so as to expose a large filtering surface, by the filtering sheet being given U-shape (in section), and air leaves through the base of the U, said base being non-glued and therefore being able to provide a large evacuation area. The end of thefilling pipe 3 is bent to impart to the injected material a direction obliquely downwards in the bag, i.e. away from the ventilating valve. It has surprisingly been found that a ventilating valve according to the invention does not tend to be quickly filled or clogged by injected material, but, on the contrary, yield efficient evacuation of air during the entire filling operation. No active sucking-out of air is necessary. When the required amount of material has been injected, thefiling pipe 3 can be pulled out of thefilling valve 5 which can be immediately sealed, for instance by means of transversely applied bands of selectively activatable sealing material, advantageously of the hot-melt type. Then, a direct, active, terminating continued evacuation of air from the bag may take place through the ventilating air, preferably by mangling of the bag. - Figs 2 and 3 illustrate an example how to modify according to the present invention a conventional valve bag of the canister type. Since valve bags of this type are well-known, merely modifications which are important to the invention will be discussed in more detail.
- Fig. 2 illustrates how an unfolded
filling valve sheet 11 and a transversely foldedfiltering valve sheet 9 are glued on each side of the bag to the underlying flat-folded bag side flaps. The glue layers of thefilling valve sheet 11 are indicated at 13, 14, and the glue layers of the lower part of the filteringvalve sheet 9 are indicated at 15. - The filtering
valve sheet 9 has itstransverse fold 17 on the outwardly facing side of the sheet. As is apparent, theglue layer 15 begins at a considerable distance from thefold 17, such that a comparatively large non-glued area of the lower part of the sheet connects with thefold 17. This also applies to the upper part of thesheet 9, see Fig. 3. - The lower part of the
filtering sheet 9 extends into the bag a shorter distance than does the upper part of the sheet. The inner edge of the lower part is indicated at 19. The innermost edge area of the lower part advantageously extends beyond the underlying side flap. Especially if this is not possible in view of the width of the bag, a corresponding recess can be formed in the side flap, thereby ensuring free exposure of the innermost edge area of the lower part of thefiltering sheet 9. - Fig. 2 schematically shows also the arrangement of additional, transverse, selectively heat-activatable
sealing agent bands filling valve sheet 11, i.e. inside the filling valve itself. - Fig. 3 shows how the bottom gluing can be carried out. It is apparent that the
bottom glue layer 23 can basically be the same for thefilling valve sheet 11 and thefiltering valve sheet 9, although additionaltransverse glue bands 25, 26 are arranged for the inner part of the filtering sheet upper part, such that this is safely glued to the bottom of the bag and thus follows this, whereby the U-shaped opening (see Fig. 1) of the ventilating valve will be facilitated. - As is apparent, also the upper part of the
filtering sheet 9 has a comparatively large non-glued area connecting with thetransverse fold 17. The non-glued areas on both sides of thetransverse fold 17 permit a large evacuation area to be formed, when the ventilating valve is opened from the inside into U-shape. - It will be appreciated that a bottom cover sheet (not shown) glued farthest out should either not cover the above-mentioned non-glued area or, non-glued, cover the same.
- As mentioned above, it is preferred that the bag is made of a tight or non-perforated material. The invention thus makes it possible to use tight plastic bags, while maintaining the ventilating effect during filling.
- When paper bags are involved, the fact that there are no perforations may confer several advantages, such as a reduced risk of broken webs in the bag-making machine and no bleeding-through.
- A more efficient evacuation of air and no perforations may permit the use of thinner bag materials.
- The use of non-perforated bags generally leads to reduced emission while emptying the bags and handling the emptied bags.
- It thus appears to be a great advantage to be able to use tight or non-perforated bags. However, it should be emphasised that if tightness or lack of perforations is not primarily necessary, the invention may in any case be used since the evacuation of air is rendered more effective, which results in certain advantages, for example, the possibility of quicker filling and simpler and lighter mangling.
Claims (10)
- A method for filling a valve bag (1) with dust-producing and/or hazardous material, the material being supplied through a bag-filling valve (5) arranged in a corner of one end of the bag, and air which accompanies the material supplied into the bag being removed through ventilating means (7) arranged in the bag, further comprising using a bag (1) of a tight material, such as non-perforated paper or plastic, said bag having ventilating means in the form of a filtering bag ventilating valve (7) in the opposite corner of said one end of the bag, said bag ventilating valve (7) being opened by an excess pressure in the bag, filling the bag by injection of material obliquely downwards in the bag, while evacuation of air occurs through the bag ventilating valve (7), and,immediately after filling, sealing the filling valve (5) and actively finally-evacuating the air from the filled bag.
- The method as claimed in claim 1, wherein the final evacuation of air comprises mangling of the filled bag (1).
- The method as claimed in claim 2, wherein mangling is carried out after sealing of the filling valve (5).
- The method as claimed in claim 1 or 2, wherein the final evacuation of air occurs before the used filling nozzle (3) or the like is removed from the filling valve (5), and the filling valve is then directly sealed.
- The method as claimed in any one of the preceding claims, further comprising using a bag (1) fitted with a bag ventilating valve (7) comprising a transversely folded filtering valve sheet (9), the sheet fold (17) facing outwards from the interior of the bag, such that the bag ventilating valve (7) can be expanded by an excess pressure in the bag, for exposing a large filtering valve sheet surface.
- A valve bag (1), especially of the so-called canister type, especially for use in connection with a method according to any one of the preceding claims, comprising a filling valve (5) in one corner of one end of the bag and a ventilating valve (7) in the other corner of said one end, the valve bag (1) being made preferably of a tight or non-perforated material, characterised in that the filling valve (5) is provided with sealing means (21,22) to be sealed after filling of the bag thereby sealing the filling valve (5), and that said ventilating valve (7) has an air-permeable, transversely folded filtering valve sheet (9), the fold (17) of which faces outwards from the interior of the bag (1) and is adapted to be expanded by an excess pressure in the bag, so as to expose a large filtering valve sheet surface.
- The valve bag as claimed in claim 6, wherein the filtering valve sheet (9) is non-glued within a substantial area on both sides of the fold (17) of the sheet, such that the filtering valve sheet (9) can assume, during evacuation of air, a configuration having a U-shaped, inwardly open section perpendicular to its fold.
- The valve bag as claimed in claim 6 or 7, wherein the lower part, facing the interior of the bag, of the filtering valve sheet (9) extends a shorter distance into the bag (1) than does its upper part facing the exterior, preferably beyond the inner edge of the turned-in bag flap or over a recess in the inner edge area of the bag flap.
- The valve bag as claimed in any one of claims 6-8, wherein the inner part of the upper part, facing the outside, of the filtering valve sheet (9) is glued to the bottom of the bag (1).
- The valve bag as claimed in any one of claims 6-9, wherein said sealing means are provided inside the filling valve (5), preferably comprising transversely applied bands (21,22) of selectively activatable sealing material.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| EP99100491A EP0922638A3 (en) | 1994-10-10 | 1995-10-10 | Method for filling a valve bag, and a valve bag |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| SE9403434 | 1994-10-10 | ||
| SE9403434A SE509957C2 (en) | 1994-10-10 | 1994-10-10 | Procedure for filling a valve bag and valve bag |
Related Child Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99100491A Division EP0922638A3 (en) | 1994-10-10 | 1995-10-10 | Method for filling a valve bag, and a valve bag |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0706940A1 EP0706940A1 (en) | 1996-04-17 |
| EP0706940B1 true EP0706940B1 (en) | 1999-07-28 |
Family
ID=20395545
Family Applications (2)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99100491A Withdrawn EP0922638A3 (en) | 1994-10-10 | 1995-10-10 | Method for filling a valve bag, and a valve bag |
| EP95850175A Expired - Lifetime EP0706940B1 (en) | 1994-10-10 | 1995-10-10 | A method of filling a valve bag and valve bag |
Family Applications Before (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP99100491A Withdrawn EP0922638A3 (en) | 1994-10-10 | 1995-10-10 | Method for filling a valve bag, and a valve bag |
Country Status (4)
| Country | Link |
|---|---|
| EP (2) | EP0922638A3 (en) |
| DE (1) | DE69511031D1 (en) |
| DK (1) | DK0706940T3 (en) |
| SE (1) | SE509957C2 (en) |
Families Citing this family (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| HUP0900208A2 (en) * | 2009-04-08 | 2010-11-29 | Zoltan Mandzsu | Packaging methods, valve bags and packages |
| DE202013102644U1 (en) * | 2013-06-19 | 2013-07-24 | Papiersackfabrik Tenax Gmbh & Co. Kg | Valve bag with ventilation devices |
| CN104309829A (en) * | 2014-09-30 | 2015-01-28 | 锐派包装技术(上海)有限公司 | Feeding nozzle structure |
| CN113306867B (en) * | 2021-06-01 | 2022-11-29 | 合肥皖燃新材料科技有限公司 | Material packaging bag and packaging device for processing asphalt fire retardant |
Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4140213A1 (en) * | 1991-12-06 | 1993-06-09 | Dy-Pack Verpackungen Gustav Dyckerhoff Gmbh, 5962 Drolshagen, De | Filler valve for filling sacks - has valve which allows air to flow out but prevents flow of material |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| FR657508A (en) * | 1928-07-13 | 1929-05-23 | Devices for evacuating air from so-called self-closing bags | |
| US2040337A (en) * | 1935-04-26 | 1936-05-12 | John A Rosmait | Moisture resistant valve bag |
-
1994
- 1994-10-10 SE SE9403434A patent/SE509957C2/en not_active IP Right Cessation
-
1995
- 1995-10-10 EP EP99100491A patent/EP0922638A3/en not_active Withdrawn
- 1995-10-10 DE DE69511031T patent/DE69511031D1/en not_active Expired - Lifetime
- 1995-10-10 DK DK95850175T patent/DK0706940T3/en active
- 1995-10-10 EP EP95850175A patent/EP0706940B1/en not_active Expired - Lifetime
Patent Citations (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE4140213A1 (en) * | 1991-12-06 | 1993-06-09 | Dy-Pack Verpackungen Gustav Dyckerhoff Gmbh, 5962 Drolshagen, De | Filler valve for filling sacks - has valve which allows air to flow out but prevents flow of material |
Also Published As
| Publication number | Publication date |
|---|---|
| SE509957C2 (en) | 1999-03-29 |
| DK0706940T3 (en) | 2000-03-27 |
| SE9403434L (en) | 1996-04-11 |
| EP0706940A1 (en) | 1996-04-17 |
| DE69511031D1 (en) | 1999-09-02 |
| EP0922638A2 (en) | 1999-06-16 |
| SE9403434D0 (en) | 1994-10-10 |
| EP0922638A3 (en) | 1999-06-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| RU2065389C1 (en) | Flexible container | |
| WO1996004768A1 (en) | Bag for microwave cooking | |
| WO1999001350A9 (en) | Carton, carton blank and method for forming the carton | |
| US4930904A (en) | Cross-bottom or block-bottom valve sack | |
| JP3561883B2 (en) | Bag with self-closing seal valve | |
| US20020079238A1 (en) | Bag with absorbent pad | |
| JP3182692B2 (en) | Self-closing bag with sealable valve | |
| US4604757A (en) | Paper sack with a valve for packaging pulverized or granular materials | |
| US4453270A (en) | Pasted valve stepped end bag | |
| EP0706940A1 (en) | A method of filling a valve bag and valve bag | |
| US5514854A (en) | Gusseted microwave popcorn bag with susceptor | |
| JP2001233353A (en) | Paper bag wit valve port for packaging powder | |
| EP1053184B1 (en) | Close sack with air exhaustion | |
| ATE178860T1 (en) | VENTABLE CROSS BOTTOM VALVE BAG | |
| US1299683A (en) | Corrugated-paper box or other container. | |
| EP0291128A1 (en) | Valve bag with venting means | |
| US4322259A (en) | Method of making a reinforced vacuum cleaner filter bag | |
| JP6509891B2 (en) | bag | |
| WO2019232603A1 (en) | Constructive arrangement in paper bag | |
| JP3360800B2 (en) | Paper bag with outer valve for powder packaging | |
| US4512788A (en) | Top loading upright vacuum cleaner bag and method of manufacturing the same | |
| JPS6013788Y2 (en) | double bottom sewing bag | |
| US4361268A (en) | Sleeve construction for a bag having a filling opening | |
| JPH03176364A (en) | Method for manufacturing powder packaging bags and powder packaging bodies | |
| KR100282686B1 (en) | Self-sealing valve bag for contents storage |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): BE DE DK ES FR GB IT SE |
|
| 17P | Request for examination filed |
Effective date: 19961015 |
|
| 17Q | First examination report despatched |
Effective date: 19970821 |
|
| RAP1 | Party data changed (applicant data changed or rights of an application transferred) |
Owner name: ASSIDOMAEN SCANDISACK A/S |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAG | Despatch of communication of intention to grant |
Free format text: ORIGINAL CODE: EPIDOS AGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAH | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOS IGRA |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): BE DE DK ES FR GB IT SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 19990728 Ref country code: FR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19990728 Ref country code: ES Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 19990728 Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19990728 |
|
| REF | Corresponds to: |
Ref document number: 69511031 Country of ref document: DE Date of ref document: 19990902 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19991019 Year of fee payment: 5 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19991028 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19991029 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DK Payment date: 19991029 Year of fee payment: 5 |
|
| EN | Fr: translation not filed | ||
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19991028 |
|
| 26N | No opposition filed | ||
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20001010 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: THE PATENT HAS BEEN ANNULLED BY A DECISION OF A NATIONAL AUTHORITY Effective date: 20001030 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EBP |
|
| EUG | Se: european patent has lapsed |
Ref document number: 95850175.1 |