EP0473499B1 - Verfahren und Einrichtung für ein Strahlschutzrohr beim Stranggiessen - Google Patents
Verfahren und Einrichtung für ein Strahlschutzrohr beim Stranggiessen Download PDFInfo
- Publication number
- EP0473499B1 EP0473499B1 EP91402296A EP91402296A EP0473499B1 EP 0473499 B1 EP0473499 B1 EP 0473499B1 EP 91402296 A EP91402296 A EP 91402296A EP 91402296 A EP91402296 A EP 91402296A EP 0473499 B1 EP0473499 B1 EP 0473499B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- tube
- tundish
- stream protection
- protection tube
- metal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Revoked
Links
- 238000009749 continuous casting Methods 0.000 title claims description 13
- 238000009434 installation Methods 0.000 title claims description 11
- 238000000034 method Methods 0.000 title claims description 7
- 230000001681 protective effect Effects 0.000 title description 16
- 239000002184 metal Substances 0.000 claims abstract description 19
- 229910001338 liquidmetal Inorganic materials 0.000 claims description 15
- 238000005266 casting Methods 0.000 claims description 5
- 238000004880 explosion Methods 0.000 abstract description 3
- 239000003570 air Substances 0.000 description 12
- 210000002816 gill Anatomy 0.000 description 8
- 230000003647 oxidation Effects 0.000 description 4
- 238000007254 oxidation reaction Methods 0.000 description 4
- 239000002893 slag Substances 0.000 description 2
- 229910000831 Steel Inorganic materials 0.000 description 1
- 239000012080 ambient air Substances 0.000 description 1
- 239000000839 emulsion Substances 0.000 description 1
- 238000010079 rubber tapping Methods 0.000 description 1
- 230000035939 shock Effects 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D41/00—Casting melt-holding vessels, e.g. ladles, tundishes, cups or the like
- B22D41/50—Pouring-nozzles
Definitions
- the present invention relates to a jet protective tube located between the ladle and the liquid metal distributor of a continuous casting installation and to a continuous casting method using such a tube.
- the flow of liquid metal between the ladle and the distributor takes place by passage through a jet protective tube.
- This tube fixed at the end of the ladle taphole, is immersed in the distributor in order to guide the jet, to avoid renitriding of the steel and its oxidation due to its contact with air, and avoid entrainment of dross and slag present on the surface of the liquid metal contained in the distributor either towards the bottom, due to the emulsion generated by the fall of the metal from the ladle towards the distributor, or towards outside the dispenser due to possible splashing due to said fall.
- the problem is as follows: - or the lower part of the jet protective tube is immersed in the liquid metal contained in the dispenser before the opening of the tap tapping hole. In this case, during the opening of said tap hole, the liquid metal of the ladle descends into the tube, compressing the air which was trapped there.
- part of the jet is not protected and is in contact with the ambient air, which causes oxidation of the liquid metal in this unprotected part.
- the subject of the invention is a jet protective tube of a continuous casting installation making it possible to remedy these drawbacks as well as a continuous casting process using such a tube.
- It relates more particularly to a jet protective tube of a continuous casting installation, characterized in particular that the lower end of this tube is provided with at least one air outlet or air outlet.
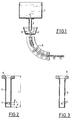
- a continuous casting installation is made up of a ladle 1 above a distributor or distributor 2. Between the ladle 1 and the distributor 2, the metal is guided by a protective jet tube 3.
- the ladle 1 of known type, is provided in its bottom with a tap hole 4, of vertical axis x-x, circular and arranged in its middle in the embodiment shown.
- the distributor 2 located under the ladle, is filled with a bath of liquid metal 8 and is provided in its bottom with a hole connected in a known manner to a continuous casting line 5.
- the jet protective tube 3 is a vertical tube of length L, of axis x-x coincident with the axis of the tap hole 4 of the bag 1.
- the device 6 is a support plate.
- the tube 3 has, in its lower part opposite the end provided with the device 6 at least one lumen or hole 7, of height h .
- the tube has two holes of rectangular shape arranged opposite one another in the same cross section of the tube.
- the tube has four circular holes distributed around the axis x-x and located in the same cross section of the tube 3.
- the tube may have gills of geometrical shapes different from those shown in FIGS. 2 and 3, and arranged differently, for example four triangular-shaped openings distributed around the periphery of the tube and located in different sections or at different levels.
- the distance d between the upper end of the nozzle, the highest when the tube has several gills arranged on different sections, and the lower end of the jet protective tube 3, is at most equal to the ferrostatic height at the overflow of the distributor used, that is to say substantially the height of the distributor.
- the jet protective tube continues to be lowered into the distributor at a speed V until the openings 7 are completely submerged in the distributor bath (Fig. 5).
- the speed of descent of the tube V is a function of the height of the tube, its section and the density of the metal being poured. It is chosen so that, when the first drop of metal arrives at the gills, the latter are about to be completely immersed in the dispenser bath. - As soon as the openings 7 are completely submerged in the distributor bath, the descent of the tube stops and the entire pocket is poured under these conditions.
- the entire jet is protected at all stages of the process, which prevents metal oxidation phenomena in the jet.
- the desired objective is therefore achieved effectively and by particularly simple and inexpensive means.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Continuous Casting (AREA)
- Manufacture And Refinement Of Metals (AREA)
- Casting Support Devices, Ladles, And Melt Control Thereby (AREA)
- Treatment Of Steel In Its Molten State (AREA)
Claims (7)
- Strahlschutzrohr (3), welches zwischen der Gießpfanne (1) und dem Zuteiler (2) für das flüssige Metall einer Stanggießeinrichtung liegt, dadurch gekennzeichnet, daß das untere Ende des Rohres (3) mit wenigstens einer Durchtrittsöffnung (7) versehen.
- Strahlschutzrohr nach Anspruch 1, dadurch gekennzeichnet, daß der Abstand d zwischen dem oberen Ende der Öffnung (7) und dem unteren Ende des Strahlschutzrohres (3) höchstens gleich der ferrostatischen Höhe am überlauf des Zuteilers (2) ist.
- Strahlschutzrohr nach Anspruch 1, dadurch gekennzeichnet, daß die Öffnung (7) rechteckig ist
- Strahlschutzrohr nach Anspruch 1, dadurch gekennzeichnet, daß die Öffnung (7) kreisförmig ist.
- Strahlschutzrohr nach Anspruch 1, dadurch gekennzeichnet, daß es wenigstens zwei regelmäßig verteilte und im gleichen Querschnitt des Rohres angeordnete Öffnungen (7) aufweist.
- Stanggießverfahren, welches ein Strahlschutzrohr nach irgendeinem der Ansprüche 1 bis 5 einsetzt, dadurch gekennzeichnent, daß
die Gießpfanne (1) über den Verteiler (2) geführt und diese Gießpfanne abgesenkt wird, bis ein unterer Abschnitt (a) des Rohres, der unter der tiefsten Öffnung (7) liegt, in das im Zuteiler enthaltene Metall eintaucht,
das Gießloch (4) geöffnet wird, das flüssige Metall im Rohr herabsteigt und die durch das Metall geschobene, im Rohr enthaldene Luft über dem Zuteiler durch die Öffnungen (7) entweicht, während das Strahlschutzrohr weiterhin in den Zuteiler abgesenkt wird, bis die Öffnungen (7) vollständig in die Schmelze des Zuteilers eingetaucht sind,
das Absenken des Rohres angehalten wird, sobald die Öffnungen (7) vollständig in die Schmelze des Zuteilers eingetaucht sind, und das Gießen der gesamten Pfanne unter diesen Bedingungen fortgesetzt wird. - Verfahren nach Anspruch 6, dadurch gekennzeichnet, daß die Geschwindigkeit (V) des Absenkens des Rohres (3) in den Verteiler so gewählt wird, daß, wenn das Metall auf Höhe der Öffnungen (7) ankommt, sich diese an dem Punkt befinden, wo sie vollständig in die Schmelze des Verteilers eingetaucht sind.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| FR9010829A FR2666257B1 (fr) | 1990-08-30 | 1990-08-30 | Tube protecteur de jet d'une installation de coulee continue et procede en comportant application. |
| FR9010829 | 1990-08-30 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0473499A1 EP0473499A1 (de) | 1992-03-04 |
| EP0473499B1 true EP0473499B1 (de) | 1994-06-22 |
Family
ID=9399968
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP91402296A Revoked EP0473499B1 (de) | 1990-08-30 | 1991-08-22 | Verfahren und Einrichtung für ein Strahlschutzrohr beim Stranggiessen |
Country Status (6)
| Country | Link |
|---|---|
| US (1) | US5180537A (de) |
| EP (1) | EP0473499B1 (de) |
| AT (1) | ATE107553T1 (de) |
| DE (1) | DE69102601T2 (de) |
| ES (1) | ES2059081T3 (de) |
| FR (1) | FR2666257B1 (de) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN109916348B (zh) * | 2019-03-21 | 2020-08-21 | 广西大学 | 一种基于立式储罐本体泄漏口处液体落地水平距离s计算模型 |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CH445034A (de) * | 1966-10-18 | 1967-10-15 | Metacon Ag | Ausgussvorrichtung |
| US3845943A (en) * | 1973-10-26 | 1974-11-05 | J Shapland | Refractory pouring tube |
| US4510191A (en) * | 1982-09-30 | 1985-04-09 | Toshiba Ceramics Co., Ltd. | Casting nozzle |
| US4662546A (en) * | 1985-07-30 | 1987-05-05 | Allegheny Ludlum Corporation | Submerged nozzle for use in the continuous casting of slabs |
| GB8624738D0 (en) * | 1986-10-15 | 1986-11-19 | British Steel Corp | Refractory pouring tube |
| US4887748A (en) * | 1986-12-29 | 1989-12-19 | J. W. Hicks, Inc. | Apparatus and method for attachment of submerged nozzle to lower plate of sliding gate valve mechanism for a continuous casting operation |
-
1990
- 1990-08-30 FR FR9010829A patent/FR2666257B1/fr not_active Expired - Lifetime
-
1991
- 1991-08-22 DE DE69102601T patent/DE69102601T2/de not_active Expired - Fee Related
- 1991-08-22 ES ES91402296T patent/ES2059081T3/es not_active Expired - Lifetime
- 1991-08-22 EP EP91402296A patent/EP0473499B1/de not_active Revoked
- 1991-08-22 AT AT91402296T patent/ATE107553T1/de not_active IP Right Cessation
- 1991-08-29 US US07/751,831 patent/US5180537A/en not_active Expired - Fee Related
Also Published As
| Publication number | Publication date |
|---|---|
| EP0473499A1 (de) | 1992-03-04 |
| DE69102601T2 (de) | 1994-11-24 |
| DE69102601D1 (de) | 1994-07-28 |
| ES2059081T3 (es) | 1994-11-01 |
| FR2666257A1 (fr) | 1992-03-06 |
| US5180537A (en) | 1993-01-19 |
| ATE107553T1 (de) | 1994-07-15 |
| FR2666257B1 (fr) | 1992-12-11 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| FR2499229A1 (fr) | Dispositif pour boucher le trou de coulee d'un recipient metallurgique | |
| EP0269180A2 (de) | Vorrichtung zum Giessen eines pastenartigen Metalles | |
| CA1302045C (fr) | Procede de moulage sous pression de pieces metalliques contenant eventuellement des fibres en ceramiques | |
| EP0847821A1 (de) | Beschickbehälter für die Aufnahme schmelzflüssigen Metalls, insbesondere Stahlschmelzen | |
| EP0473499A1 (de) | Verfahren und Einrichtung für ein Strahlschutzrohr beim Stranggiessen | |
| FR2568152A1 (fr) | Perfectionnement apporte aux busettes de coulee continue | |
| EP0446152B1 (de) | Paket zum Einführen von Leichtmetall in Aluminiumlegierungsschmelze | |
| FR2517574A1 (fr) | Busette de coulee et application de cette busette | |
| EP0498684B1 (de) | Ausstosseinrichtung für eine Giessschutzrohr-Trageinrichtung in eine Stranggiessvorrichtung | |
| EP0120045B1 (de) | Verfahren zur überwachung und zum öffnen der giessöffnungen von flüssige metalle enthaltenden gefässen und vorrichtung zur durchführung des verfahrens | |
| EP0213042A2 (de) | Vorrichtung zum Schutz eines flüssigen Giesstrahls gegen Oxydation und/oder Nitrierung | |
| FR2642679A3 (fr) | Dispositif d'elimination des inclusions non metalliques dans un repartiteur de coulee continue de l'acier | |
| EP0203979B1 (de) | Verbesserungen an giesspfannen für flüssige metalle | |
| EP0242347A2 (de) | Vorrichtung zum Giessen einer flüssig-festen Mischung | |
| FR2716819A1 (fr) | Procédé et dispositif de coulée. | |
| CA1119377A (fr) | Procede de coulee continue centrifuge electromagnetique des metaux en fusion | |
| FR2728491A1 (fr) | Dispositif de coulee d'un metal liquide avec injection d'un gaz inerte dans le metal liquide en cours de coulee | |
| EP0528724B1 (de) | Vorrichtung zum automatischen Entschlacken des Giessstrahlschutzrohres beim Stranggiessen | |
| EP0030910B1 (de) | Tauchrohre für elektrorotierendes Stranggiessen von Metallen | |
| FR2669567A1 (fr) | Dispositif d'ouverture et de fermeture d'un recipient contenant un metal a l'etat liquide. | |
| FR2651160A1 (fr) | Procede et dispositif pour couler des barres metalliques ou analogues. | |
| BE1000227A6 (fr) | Dispositif permettant de couler un metal en phase pateuse. | |
| CA1206752A (fr) | Procede et dispositif pour vidanger des recipients metallurgiques | |
| EP0943380A1 (de) | Verfahren und Vorrichtung zum Stranggiessen von Metallen | |
| FR2659880A1 (fr) | Dispositif de liaison entre un recipient metallurgique contenant un metal liquide et une lingotiere. |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 19911125 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE CH DE DK ES FR GB GR IT LI LU NL SE |
|
| 17Q | First examination report despatched |
Effective date: 19931013 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE CH DE DK ES FR GB GR IT LI LU NL SE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Effective date: 19940622 |
|
| REF | Corresponds to: |
Ref document number: 107553 Country of ref document: AT Date of ref document: 19940715 Kind code of ref document: T |
|
| ITF | It: translation for a ep patent filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: CH Payment date: 19940714 Year of fee payment: 4 |
|
| GBT | Gb: translation of ep patent filed (gb section 77(6)(a)/1977) |
Effective date: 19940622 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: AT Payment date: 19940722 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19940727 Year of fee payment: 4 |
|
| REF | Corresponds to: |
Ref document number: 69102601 Country of ref document: DE Date of ref document: 19940728 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: LU Payment date: 19940731 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: ES Payment date: 19940801 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 19940816 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19940829 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 19940831 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: BE Payment date: 19940909 Year of fee payment: 4 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 19940923 |
|
| EPTA | Lu: last paid annual fee | ||
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2059081 Country of ref document: ES Kind code of ref document: T3 |
|
| EAL | Se: european patent in force in sweden |
Ref document number: 91402296.7 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| 26 | Opposition filed |
Opponent name: DIDIER-WERKE AG Effective date: 19950310 |
|
| 26 | Opposition filed |
Opponent name: VESUVIUS FRANCE S.A. Effective date: 19950320 Opponent name: DIDIER-WERKE AG Effective date: 19950310 |
|
| NLR1 | Nl: opposition has been filed with the epo |
Opponent name: DIDIER WERKE AG |
|
| NLR1 | Nl: opposition has been filed with the epo |
Opponent name: VESUVIUS FRANCE S.A. |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19950822 Ref country code: GB Effective date: 19950822 Ref country code: AT Effective date: 19950822 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Effective date: 19950823 Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19950823 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19950831 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19950831 Ref country code: BE Effective date: 19950831 |
|
| PLBF | Reply of patent proprietor to notice(s) of opposition |
Free format text: ORIGINAL CODE: EPIDOS OBSO |
|
| BERE | Be: lapsed |
Owner name: SOLLAC Effective date: 19950831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Effective date: 19960301 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 19950822 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Effective date: 19960430 |
|
| NLV4 | Nl: lapsed or anulled due to non-payment of the annual fee |
Effective date: 19960301 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Effective date: 19960501 |
|
| EUG | Se: european patent has lapsed |
Ref document number: 91402296.7 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| RDAH | Patent revoked |
Free format text: ORIGINAL CODE: EPIDOS REVO |
|
| RDAG | Patent revoked |
Free format text: ORIGINAL CODE: 0009271 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT REVOKED |
|
| 27W | Patent revoked |
Effective date: 19960808 |