EP0293961A1 - Casting method and apparatus therefor - Google Patents
Casting method and apparatus therefor Download PDFInfo
- Publication number
- EP0293961A1 EP0293961A1 EP88200895A EP88200895A EP0293961A1 EP 0293961 A1 EP0293961 A1 EP 0293961A1 EP 88200895 A EP88200895 A EP 88200895A EP 88200895 A EP88200895 A EP 88200895A EP 0293961 A1 EP0293961 A1 EP 0293961A1
- Authority
- EP
- European Patent Office
- Prior art keywords
- mould
- chamber
- pressure
- casting
- molten metal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 25
- 238000005266 casting Methods 0.000 title claims abstract description 19
- 229910052751 metal Inorganic materials 0.000 claims abstract description 22
- 239000002184 metal Substances 0.000 claims abstract description 22
- 239000012530 fluid Substances 0.000 claims abstract description 11
- 238000007711 solidification Methods 0.000 claims abstract description 8
- 230000008023 solidification Effects 0.000 claims abstract description 8
- XKRFYHLGVUSROY-UHFFFAOYSA-N Argon Chemical compound [Ar] XKRFYHLGVUSROY-UHFFFAOYSA-N 0.000 claims description 8
- 230000010355 oscillation Effects 0.000 claims description 7
- 238000004519 manufacturing process Methods 0.000 claims description 5
- IJGRMHOSHXDMSA-UHFFFAOYSA-N Atomic nitrogen Chemical compound N#N IJGRMHOSHXDMSA-UHFFFAOYSA-N 0.000 claims description 4
- 229910052786 argon Inorganic materials 0.000 claims description 4
- 239000001307 helium Substances 0.000 claims description 2
- 229910052734 helium Inorganic materials 0.000 claims description 2
- SWQJXJOGLNCZEY-UHFFFAOYSA-N helium atom Chemical compound [He] SWQJXJOGLNCZEY-UHFFFAOYSA-N 0.000 claims description 2
- 238000002844 melting Methods 0.000 claims description 2
- 230000008018 melting Effects 0.000 claims description 2
- 229910052757 nitrogen Inorganic materials 0.000 claims description 2
- 238000005086 pumping Methods 0.000 claims description 2
- 229910000838 Al alloy Inorganic materials 0.000 claims 1
- 229910000531 Co alloy Inorganic materials 0.000 claims 1
- 229910000881 Cu alloy Inorganic materials 0.000 claims 1
- 229910000640 Fe alloy Inorganic materials 0.000 claims 1
- 229910001030 Iron–nickel alloy Inorganic materials 0.000 claims 1
- 239000007789 gas Substances 0.000 description 4
- 238000010438 heat treatment Methods 0.000 description 4
- 238000009413 insulation Methods 0.000 description 4
- 230000015572 biosynthetic process Effects 0.000 description 3
- 238000010276 construction Methods 0.000 description 3
- 210000001787 dendrite Anatomy 0.000 description 3
- 229910001338 liquidmetal Inorganic materials 0.000 description 3
- 230000001681 protective effect Effects 0.000 description 3
- 229910045601 alloy Inorganic materials 0.000 description 2
- 239000000956 alloy Substances 0.000 description 2
- 239000002826 coolant Substances 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 230000003534 oscillatory effect Effects 0.000 description 2
- YPFNIPKMNMDDDB-UHFFFAOYSA-K 2-[2-[bis(carboxylatomethyl)amino]ethyl-(2-hydroxyethyl)amino]acetate;iron(3+) Chemical compound [Fe+3].OCCN(CC([O-])=O)CCN(CC([O-])=O)CC([O-])=O YPFNIPKMNMDDDB-UHFFFAOYSA-K 0.000 description 1
- 230000005540 biological transmission Effects 0.000 description 1
- 239000000919 ceramic Substances 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 229910017052 cobalt Inorganic materials 0.000 description 1
- 239000010941 cobalt Substances 0.000 description 1
- GUTLYIVDDKVIGB-UHFFFAOYSA-N cobalt atom Chemical compound [Co] GUTLYIVDDKVIGB-UHFFFAOYSA-N 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 230000001627 detrimental effect Effects 0.000 description 1
- 238000011065 in-situ storage Methods 0.000 description 1
- 230000006698 induction Effects 0.000 description 1
- 238000002955 isolation Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 238000005096 rolling process Methods 0.000 description 1
- 229910000601 superalloy Inorganic materials 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D27/00—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting
- B22D27/09—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting by using pressure
- B22D27/13—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting by using pressure making use of gas pressure
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D27/00—Treating the metal in the mould while it is molten or ductile ; Pressure or vacuum casting
- B22D27/08—Shaking, vibrating, or turning of moulds
Definitions
- the present invention relates to a method and apparatus for casting of articles.
- the method comprises casting molten metal into a mould under reduced pressure or under a protective atmosphere in a first chamber and then immediately withdrawing the filled mould containing the molten metal into a second chamber and increasing the pressure in the second chamber with a fluid up to a maximum pressure of 7 MPa until at least partial solidification has occurred.
- Apparatus is also described for carrying out the method of the invention.
- the method and apparatus described in co-pending DG55 is particularly suitable for gas turbine engine components such as blades and nozzle guide vanes, for example, which are cast in gas permeable ceramic moulds.
- gas turbine engine components such as blades and nozzle guide vanes, for example, which are cast in gas permeable ceramic moulds.
- Such components as blades possess substantial differences in section between the root and airfoil portions which leads, in conventional casting methods for components having equiaxed grain structures, to shrinkage porosity in the thinner airfoil portion.
- Such components include turbine wheels for gas turbine engines and turbochargers, for example, where a multiplicity of airfoils are cast integrally with a hub or disc portion.
- the method and apparatus of the present invention provide components which have large section differences with both an equiaxed grain structure and reduced levels of porosity.
- a method for the production of cast components comprises the step of filling a mould of the desired component with molten metal in a first chamber, withdrawing the filled mould into a second chamber, isolating the second chamber from the first chamber with regard to pressure, pressurising the second chamber with a fluid up to a maximum pressure of 7 MPa and oscillating the filled mould whilst under pressure until at least partial solidification has occurred.
- the metal may be cast in the first chamber under reduced pressure or under a protective atmosphere.
- the mould may be preheated whilst in the first chamber rather than preheating in an external preheating furnace. Greater control and flexibility of preheating is obtainable with in-situ preheating by means of, for example, radiant heaters.
- the pressurising fluid may be a gas having little or no chemical reaction with the molten metal.
- examples may include argon, helium and nitrogen.
- the pressure may be applied to the filled mould in the mould chamber within 60 seconds of the completion of pouring and more preferably within 30 seconds.
- the mould may be oscillated about an axis which is eccentric to the axis of the component being cast.
- the mould may be oscillated within a frequency range of from 5 to 500 cycles per minute.
- the amplitude of oscillation may lie in the range from 5° to 360° in any one cycle or may be in excess of one complete revolution of the mould.
- Frequency and amplitude of oscillation will vary with component dimensions and geometry and furthermore may also vary during the solidification process itself and be affected by the alloy being cast.
- apparatus for the production of cast components comprises a casting chamber, metal melting and pouring means, a mould chamber adjacent the casting chamber and connected thereto by valve means of sufficient size to allow a mould to pass therethrough, mould moving means to move the mould between the casting chamber and the mould chamber, pressurising means for pressurising the mould chamber with a fluid and means for oscillating the mould in the mould chamber.
- the casting chamber may also have vacuum pump means associated with it, as may the mould chamber, for producing a reduced pressure within the chambers.
- the chambers may be provided with suitable connections for producing a gaseous protective atmosphere such as with argon, for example, within the chambers.
- the apparatus is shown generally at 10 and comprises a vacuum casting chamber 11 which includes a port 12 connected to a vacuum pump (not shown). Contained in the chamber 11 is a coil box assembly 13 having induction heating coils (not shown) and crucible 14; the assembly 13 being mounted such that it may be tilted to pour the molten metal 15 in known manner.
- the chamber also includes a port 16 and vacuum lock 17 to enable the crucible 14 to be recharged with fresh metal whilst under vacuum.
- an aperture 21 In the bottom wall 20 of the chamber 11 is an aperture 21 of sufficient size to allow a mould assembly 22, having an axis 22a, to pass therethrough.
- a mould heating chamber 23 which comprises an outer insulating box 24 having contained therein known radiant heating means 25 having the appropriate power supply and control means (not shown) attached thereto.
- an aperture having a pouring tube 27 therein to guide the molten metal into the mould 22 on pouring.
- a mould chamber 30 below the vacuum chamber 11 is a mould chamber 30.
- the mould chamber 30 is attached in sealed engagement to the bottom wall 20 of the casting chamber 11.
- the chamber 30 may be isolated from the chamber 11 by means of the isolation valve 31 and seal 32.
- the valve 31 may be moved between the open position ( Figure 1) and the closed position ( Figure 2) by suitable known remotely operated control means (not shown). Cooling passages 33 are provided around the chamber wall.
- the chamber 30 has a door 34 in the wall to allow positioning and subsequent removal of the mould 22, the door 34 is sealable to the chamber wall 35. Also provided in the chamber wall 35 is a vacuum pumping port 36 connected to a vacuum pump (not shown) via a valve 37. A further port 38 in the wall 35 is provided to supply fluid under pressure from a fluid supply source (not shown) via a valve 39.
- the mould 22 is mounted on a table 40 but insulated therefrom by an insulation block 41.
- the table 40 is itself mounted on a movable ram 42 having an axis 43 and which ram may slide in sealed engagement with the bottom wall 45 of the chamber 30 and also rotate or oscillate in sealed engagement therewith.
- a bearing 46 in the bottom wall 45 supports the ram in both sliding and oscillatory movement.
- the ram 42 also includes passages 48 for provision of coolant.
- a second bearing 49 and a manifold 50 to connect coolant pipes 51, 52 to the ram and allow oscillatory movement.
- a pulley wheel 54 is mounted on the lower end of the ram 42 and which pulley wheel is drivably connected to a second pulley wheel 55 by a transmission belt 56.
- the pulley wheel 55 is driven by an electric motor 58 which has appropriate power supplies (not shown) and control means (not shown).
- the motor 58 and bearing 49 are both mounted on a platform 60 which is itself mounted on a ram 61.
- the platform 60 may be varied in height relative to the bottom wall 45 of the chamber 30.
- the chamber 11 is pumped down to a pressure appropriate to the requirements of the alloy being cast.
- the valve 31 is closed against the seal 32 and the ram retracted to its position within the chamber 30.
- the mould 22 is placed and secured on the insulation block 41, the door 34 closed and sealed and the chamber 30 pumped down to a pressure in the region of that in chamber 11.
- the valve 31 is opened and the ram 42 elevated to move the mould 22 into the mould heating chamber 23.
- the mould is heated by the radiant heaters 25 to a desired temperature and once at the desired temperature molten metal 15 at a a second desired temperature is poured from the assembly 13 into the mould 33 via the pouring tube 27.
- the filled mould is immediately withdrawn from the chamber 23 into the chamber 30 and the valve 31 is closed against the seal 32 whereupon the valve 37 is closed and the valve 39 opened to pressurise the chamber 30 with fluid such as argon for example.
- the pressure may be brought to bear against the molten metal in a time of less than 20 seconds and may be raised to a maximum pressure of about 7 MPa.
- the filled mould 22 is now oscillated about the ram axis 43 at a frequency of 280 cycles/min. and an amplitude of 70°.
- the metal in the mould in the thicker sections which comprises a mixture of liquid metal and growing metal dendrites, is aggitated and causes the growing dendrites to be broken up thus preventing the formation of undesirable, coarse columnar grains.
- the pressure within the chamber 30 assists in the feeding of liquid metal to the solidifying portions to eliminate or minimise the formation of shrinkage porosity. Oscillation frequency and amplitude may be varied during the course of solidification and may only be applied for part of the time required to achieve complete solidification. Similarly the pressure may be released before complete solidification has occurred.
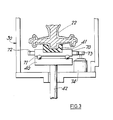
- Figure 3 shows an alternative construction of drive for oscillating the mould 22.
- the ram 42 does not itself oscillate.
- a carrier 70 which is free to rotate on the table 40 supported by a rolling element bearing 71.
- a gear toothed ring 72 On the outer periphery of the carier 70 is a gear toothed ring 72 which, when the ram 42 is lowered to its lowermost extent, meshes with a gear pinion 73 driven by an electric motor 74.
- the motor 74 is connected to suitable control apparatus (not shown) situated outside the chamber 30.
- the article being cast is a turbine disc and blade unit having rotational symmetry. Such symmetry is not necessary as any article which has widely different section thicknesses included therein may be cast by the method and apparatus of the present invention.
- the ram 42 may be elevated by electrical or hydraulic means, for example.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Turbine Rotor Nozzle Sealing (AREA)
Abstract
Description
- The present invention relates to a method and apparatus for casting of articles.
- In our co-pending patent application DG55 of even filing date herewith and claiming priority from British patent application No 8712742 filed on 30 May 1987, a method and apparatus are described for the production of cast components having an equiaxed grain structure and reduced levels of shrinkage porosity.
- The method comprises casting molten metal into a mould under reduced pressure or under a protective atmosphere in a first chamber and then immediately withdrawing the filled mould containing the molten metal into a second chamber and increasing the pressure in the second chamber with a fluid up to a maximum pressure of 7 MPa until at least partial solidification has occurred. Apparatus is also described for carrying out the method of the invention.
- The method and apparatus described in co-pending DG55 is particularly suitable for gas turbine engine components such as blades and nozzle guide vanes, for example, which are cast in gas permeable ceramic moulds. Such components as blades, for example, possess substantial differences in section between the root and airfoil portions which leads, in conventional casting methods for components having equiaxed grain structures, to shrinkage porosity in the thinner airfoil portion.
- The method described in co-pending DG55 ensures enhanced feeding of liquid metal to solidifying regions by pressurisation and thus producing reduced levels of porosity.
- There is a need, however, to produce components which have very considerable differences in section.
- Such components include turbine wheels for gas turbine engines and turbochargers, for example, where a multiplicity of airfoils are cast integrally with a hub or disc portion.
- In such components there is not only a problem with porosity in the thinner airfoil portions but there is an additional problem with the grain structure in the hub portion. Because of the generally thick and relatively extensive section of the hub portion large columnar grains tend to grow unchecked. Such grain structures are detrimental to the mechanical properties of the hub which needs to be able to withstand very high forces during operation. An equiaxed grain structure in the hub is highly desirable. It is known to prevent the formation of columnar grains by oscillating the filled mould about an axis eccentric to the component axis. Such oscillation causes mass movement within the solidifying mushy metal and breaks up the growing metal dendrites before they become too large and firmly set as growing columnar grains. A generally equiaxed grain structure is thus produced.
- The method and apparatus of the present invention provide components which have large section differences with both an equiaxed grain structure and reduced levels of porosity.
- According to a first aspect of the present invention a method for the production of cast components comprises the step of filling a mould of the desired component with molten metal in a first chamber, withdrawing the filled mould into a second chamber, isolating the second chamber from the first chamber with regard to pressure, pressurising the second chamber with a fluid up to a maximum pressure of 7 MPa and oscillating the filled mould whilst under pressure until at least partial solidification has occurred.
- In the case of turbine components cast from iron-, nickel- or cobalt-based superalloys the metal may be cast in the first chamber under reduced pressure or under a protective atmosphere.
- Preferably the mould may be preheated whilst in the first chamber rather than preheating in an external preheating furnace. Greater control and flexibility of preheating is obtainable with in-situ preheating by means of, for example, radiant heaters.
- Preferably the pressurising fluid may be a gas having little or no chemical reaction with the molten metal. Examples may include argon, helium and nitrogen.
- Preferably the pressure may be applied to the filled mould in the mould chamber within 60 seconds of the completion of pouring and more preferably within 30 seconds.
- The mould may be oscillated about an axis which is eccentric to the axis of the component being cast.
- The mould may be oscillated within a frequency range of from 5 to 500 cycles per minute.
- The amplitude of oscillation may lie in the range from 5° to 360° in any one cycle or may be in excess of one complete revolution of the mould.
- Frequency and amplitude of oscillation will vary with component dimensions and geometry and furthermore may also vary during the solidification process itself and be affected by the alloy being cast.
- According to a second aspect of the present invention apparatus for the production of cast components comprises a casting chamber, metal melting and pouring means, a mould chamber adjacent the casting chamber and connected thereto by valve means of sufficient size to allow a mould to pass therethrough, mould moving means to move the mould between the casting chamber and the mould chamber, pressurising means for pressurising the mould chamber with a fluid and means for oscillating the mould in the mould chamber.
- The casting chamber may also have vacuum pump means associated with it, as may the mould chamber, for producing a reduced pressure within the chambers.
- Alternatively or additionally the chambers may be provided with suitable connections for producing a gaseous protective atmosphere such as with argon, for example, within the chambers.
- In order that the present invention may be more fully understood an example will now be described by way of illustration only with reference to the accompanying drawings, of which:
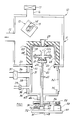
- Figure 1 shows a schematic section through apparatus according to the present invention prior to casting metal into the mould;
- Figure 2 shows part of the apparatus of Figure 1 after casting; and
- Figure 3 which shows a section through an alternative construction of apparatus for oscillating the mould.
- Referring now to Figures 1 and 2 and where the same features are denoted by common reference numerals. The apparatus is shown generally at 10 and comprises a vacuum casting chamber 11 which includes a
port 12 connected to a vacuum pump (not shown). Contained in the chamber 11 is acoil box assembly 13 having induction heating coils (not shown) andcrucible 14; theassembly 13 being mounted such that it may be tilted to pour themolten metal 15 in known manner. The chamber also includes aport 16 andvacuum lock 17 to enable thecrucible 14 to be recharged with fresh metal whilst under vacuum. In thebottom wall 20 of the chamber 11 is anaperture 21 of sufficient size to allow amould assembly 22, having anaxis 22a, to pass therethrough. Above and surrounding theaperture 21 is amould heating chamber 23 which comprises anouter insulating box 24 having contained therein known radiant heating means 25 having the appropriate power supply and control means (not shown) attached thereto. In the top of theinsulation box 24 is an aperture having apouring tube 27 therein to guide the molten metal into themould 22 on pouring. Below the vacuum chamber 11 is amould chamber 30. Themould chamber 30 is attached in sealed engagement to thebottom wall 20 of the casting chamber 11. Thechamber 30 may be isolated from the chamber 11 by means of theisolation valve 31 andseal 32. Thevalve 31 may be moved between the open position (Figure 1) and the closed position (Figure 2) by suitable known remotely operated control means (not shown).Cooling passages 33 are provided around the chamber wall. Thechamber 30 has adoor 34 in the wall to allow positioning and subsequent removal of themould 22, thedoor 34 is sealable to thechamber wall 35. Also provided in thechamber wall 35 is avacuum pumping port 36 connected to a vacuum pump (not shown) via avalve 37. Afurther port 38 in thewall 35 is provided to supply fluid under pressure from a fluid supply source (not shown) via avalve 39. Themould 22 is mounted on a table 40 but insulated therefrom by aninsulation block 41. The table 40 is itself mounted on amovable ram 42 having anaxis 43 and which ram may slide in sealed engagement with thebottom wall 45 of thechamber 30 and also rotate or oscillate in sealed engagement therewith. Abearing 46 in thebottom wall 45 supports the ram in both sliding and oscillatory movement. Theram 42 also includespassages 48 for provision of coolant. At the lower end of theram 42 is a second bearing 49 and amanifold 50 to connectcoolant pipes pulley wheel 54 is mounted on the lower end of theram 42 and which pulley wheel is drivably connected to asecond pulley wheel 55 by atransmission belt 56. Thepulley wheel 55 is driven by anelectric motor 58 which has appropriate power supplies (not shown) and control means (not shown). Themotor 58 andbearing 49 are both mounted on aplatform 60 which is itself mounted on aram 61. Theplatform 60 may be varied in height relative to thebottom wall 45 of thechamber 30. - In operation the chamber 11 is pumped down to a pressure appropriate to the requirements of the alloy being cast. The
valve 31 is closed against theseal 32 and the ram retracted to its position within thechamber 30. Themould 22 is placed and secured on theinsulation block 41, thedoor 34 closed and sealed and thechamber 30 pumped down to a pressure in the region of that in chamber 11. Thevalve 31 is opened and theram 42 elevated to move themould 22 into themould heating chamber 23. The mould is heated by theradiant heaters 25 to a desired temperature and once at the desired temperaturemolten metal 15 at a a second desired temperature is poured from theassembly 13 into themould 33 via thepouring tube 27. The filled mould is immediately withdrawn from thechamber 23 into thechamber 30 and thevalve 31 is closed against theseal 32 whereupon thevalve 37 is closed and thevalve 39 opened to pressurise thechamber 30 with fluid such as argon for example. The pressure may be brought to bear against the molten metal in a time of less than 20 seconds and may be raised to a maximum pressure of about 7 MPa. The filledmould 22 is now oscillated about theram axis 43 at a frequency of 280 cycles/min. and an amplitude of 70°. Since theaxis 22a of the mould is eccentric to theaxis 43 the metal in the mould in the thicker sections, and which comprises a mixture of liquid metal and growing metal dendrites, is aggitated and causes the growing dendrites to be broken up thus preventing the formation of undesirable, coarse columnar grains. The pressure within thechamber 30 assists in the feeding of liquid metal to the solidifying portions to eliminate or minimise the formation of shrinkage porosity. Oscillation frequency and amplitude may be varied during the course of solidification and may only be applied for part of the time required to achieve complete solidification. Similarly the pressure may be released before complete solidification has occurred. - Figure 3 shows an alternative construction of drive for oscillating the
mould 22. In this construction theram 42 does not itself oscillate. Interposed between the ram table 40 and theinsulation block 41 is acarrier 70 which is free to rotate on the table 40 supported by a rolling element bearing 71. On the outer periphery of thecarier 70 is agear toothed ring 72 which, when theram 42 is lowered to its lowermost extent, meshes with agear pinion 73 driven by anelectric motor 74. Themotor 74 is connected to suitable control apparatus (not shown) situated outside thechamber 30. - In the examples given above the article being cast is a turbine disc and blade unit having rotational symmetry. Such symmetry is not necessary as any article which has widely different section thicknesses included therein may be cast by the method and apparatus of the present invention.
- Many modifications may be made to the embodiment shown. Such modifications may relate to the type of valve employed to seal the casting chamber from the mould chamber and to the method and precise apparatus used to move the ram and mould between chambers and also the means used to oscillate the mould.
- The
ram 42 may be elevated by electrical or hydraulic means, for example.
Claims (14)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| GB8712743 | 1987-05-30 | ||
| GB878712743A GB8712743D0 (en) | 1987-05-30 | 1987-05-30 | Casting method |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0293961A1 true EP0293961A1 (en) | 1988-12-07 |
| EP0293961B1 EP0293961B1 (en) | 1991-08-14 |
Family
ID=10618177
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19880200895 Expired EP0293961B1 (en) | 1987-05-30 | 1988-05-06 | Casting method and apparatus therefor |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP0293961B1 (en) |
| DE (1) | DE3864194D1 (en) |
| GB (2) | GB8712743D0 (en) |
Cited By (15)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EA000040B1 (en) * | 1995-06-20 | 1998-02-26 | Абб Рисерч Лтд | Casting method in vacuum chamber and apparatus therefor |
| WO1998045071A1 (en) * | 1997-04-03 | 1998-10-15 | Yasui, Shouzui | Method and casting device for precision casting |
| EP0897769A1 (en) * | 1997-08-07 | 1999-02-24 | Howmet Research Corporation | Mold heating vacuum casting furnace |
| EP1031391A1 (en) * | 1999-02-22 | 2000-08-30 | Howmet Research Corporation | Anti-swirl mold pour cup and casting method |
| EP1048759A1 (en) * | 1999-04-28 | 2000-11-02 | Howmet Research Corporation | Horizontal directional solidification |
| US6257311B1 (en) | 1999-04-28 | 2001-07-10 | Howmet Research Corporation | Horizontal directional solidification |
| US6263951B1 (en) | 1999-04-28 | 2001-07-24 | Howmet Research Corporation | Horizontal rotating directional solidification |
| WO2006098382A1 (en) | 2005-03-15 | 2006-09-21 | The Japan Steel Works, Ltd. | Method of casting and casting apparatus |
| US7712511B2 (en) | 2005-03-15 | 2010-05-11 | The Japan Steel Works, Ltd. | Casting method and casting apparatus |
| FR2976594A1 (en) * | 2011-06-16 | 2012-12-21 | Inst Polytechnique Grenoble | Installation, useful for crystallization of silicon that is present in molten state in crucible e.g. hot and cold crucibles, comprises unit for imparting periodic oscillation motion to crucible so as to ensure mixing of the molten silicon |
| CN103231017A (en) * | 2013-04-07 | 2013-08-07 | 上海交通大学 | High-temperature alloy complex thin-wall casting precise casting device |
| WO2015116361A1 (en) | 2014-01-28 | 2015-08-06 | United Technologies Corporation | Casting apparatus and method for forming multi-textured, single crystal microstructure |
| CN105834409A (en) * | 2016-05-20 | 2016-08-10 | 河南理工大学 | Integrated preparing and forming device for magnesium alloy thin-walled pieces |
| CN111112587A (en) * | 2019-12-30 | 2020-05-08 | 江苏奇纳新材料科技有限公司 | Method for reducing secondary shrinkage cavity of high-temperature alloy master alloy |
| CN117020157A (en) * | 2023-07-26 | 2023-11-10 | 潍坊博源动力科技有限公司 | Vibration pressurizing fine-grain casting equipment and manufacturing process |
Families Citing this family (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5261480A (en) * | 1990-12-13 | 1993-11-16 | Sulzer-Mtu Casting Technology Gmbh | Process and apparatus for repair of drive blades such as turbine blades |
| CN105478671A (en) * | 2015-12-18 | 2016-04-13 | 贵州安吉航空精密铸造有限责任公司 | Microseismic casting process for aluminum alloy precision-investment casting |
| CN110804713B (en) * | 2019-11-14 | 2022-04-15 | 青海晶和节能环保技术服务有限公司 | Hydraulic pump valve body machining process |
Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3568752A (en) * | 1968-12-05 | 1971-03-09 | Univ Ohio State | Method for controlling the as-cast grain structure of solidified materials |
| GB1356890A (en) * | 1971-07-14 | 1974-06-19 | Leybold Heraeus Verwaltung | Directed solidification casting |
| FR2255983A1 (en) * | 1973-12-26 | 1975-07-25 | United Aircraft Corp | |
| GB1472288A (en) * | 1974-05-01 | 1977-05-04 | Tuchkevich N | Method of producing metal ingots |
| DE3220744A1 (en) * | 1982-06-02 | 1983-12-08 | Leybold-Heraeus GmbH, 5000 Köln | Melting and casting plant for vacuum or protective gas operation with at least two chambers |
| DE3603310A1 (en) * | 1986-02-04 | 1987-08-06 | Leybold Heraeus Gmbh & Co Kg | Method and apparatus for the casting of mouldings with subsequent isostatic compression |
-
1987
- 1987-05-30 GB GB878712743A patent/GB8712743D0/en active Pending
-
1988
- 1988-05-05 GB GB8810632A patent/GB2205262B/en not_active Expired - Fee Related
- 1988-05-06 DE DE8888200895T patent/DE3864194D1/en not_active Expired - Fee Related
- 1988-05-06 EP EP19880200895 patent/EP0293961B1/en not_active Expired
Patent Citations (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3568752A (en) * | 1968-12-05 | 1971-03-09 | Univ Ohio State | Method for controlling the as-cast grain structure of solidified materials |
| GB1356890A (en) * | 1971-07-14 | 1974-06-19 | Leybold Heraeus Verwaltung | Directed solidification casting |
| FR2255983A1 (en) * | 1973-12-26 | 1975-07-25 | United Aircraft Corp | |
| GB1472288A (en) * | 1974-05-01 | 1977-05-04 | Tuchkevich N | Method of producing metal ingots |
| DE3220744A1 (en) * | 1982-06-02 | 1983-12-08 | Leybold-Heraeus GmbH, 5000 Köln | Melting and casting plant for vacuum or protective gas operation with at least two chambers |
| DE3603310A1 (en) * | 1986-02-04 | 1987-08-06 | Leybold Heraeus Gmbh & Co Kg | Method and apparatus for the casting of mouldings with subsequent isostatic compression |
Cited By (23)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EA000040B1 (en) * | 1995-06-20 | 1998-02-26 | Абб Рисерч Лтд | Casting method in vacuum chamber and apparatus therefor |
| WO1998045071A1 (en) * | 1997-04-03 | 1998-10-15 | Yasui, Shouzui | Method and casting device for precision casting |
| US6253828B1 (en) * | 1997-04-03 | 2001-07-03 | Shouzui Yasui | Method and casting device for precision casting |
| CN1072071C (en) * | 1997-04-03 | 2001-10-03 | 安井章瑞 | Method of precision casting and casting equipment |
| EP0897769A1 (en) * | 1997-08-07 | 1999-02-24 | Howmet Research Corporation | Mold heating vacuum casting furnace |
| EP1031391A1 (en) * | 1999-02-22 | 2000-08-30 | Howmet Research Corporation | Anti-swirl mold pour cup and casting method |
| EP1048759A1 (en) * | 1999-04-28 | 2000-11-02 | Howmet Research Corporation | Horizontal directional solidification |
| US6257311B1 (en) | 1999-04-28 | 2001-07-10 | Howmet Research Corporation | Horizontal directional solidification |
| US6263951B1 (en) | 1999-04-28 | 2001-07-24 | Howmet Research Corporation | Horizontal rotating directional solidification |
| EP1859879A4 (en) * | 2005-03-15 | 2009-03-04 | Japan Steel Works Ltd | METHOD OF CASTING AND CASTING DEVICE |
| US7712511B2 (en) | 2005-03-15 | 2010-05-11 | The Japan Steel Works, Ltd. | Casting method and casting apparatus |
| WO2006098382A1 (en) | 2005-03-15 | 2006-09-21 | The Japan Steel Works, Ltd. | Method of casting and casting apparatus |
| FR2976594A1 (en) * | 2011-06-16 | 2012-12-21 | Inst Polytechnique Grenoble | Installation, useful for crystallization of silicon that is present in molten state in crucible e.g. hot and cold crucibles, comprises unit for imparting periodic oscillation motion to crucible so as to ensure mixing of the molten silicon |
| CN103231017B (en) * | 2013-04-07 | 2015-10-28 | 上海交通大学 | A kind of high temperature alloy complex thin wall castings hot investment casting device |
| CN103231017A (en) * | 2013-04-07 | 2013-08-07 | 上海交通大学 | High-temperature alloy complex thin-wall casting precise casting device |
| US10150159B2 (en) | 2014-01-28 | 2018-12-11 | United Technologies Corporation | Casting apparatus and method for forming multi-textured, single crystal microstructure |
| EP3099439A4 (en) * | 2014-01-28 | 2017-09-06 | United Technologies Corporation | Casting apparatus and method for forming multi-textured, single crystal microstructure |
| WO2015116361A1 (en) | 2014-01-28 | 2015-08-06 | United Technologies Corporation | Casting apparatus and method for forming multi-textured, single crystal microstructure |
| EP3685937A1 (en) * | 2014-01-28 | 2020-07-29 | United Technologies Corporation | Casting article and method for forming multi-textured, single crystal microstructure |
| CN105834409A (en) * | 2016-05-20 | 2016-08-10 | 河南理工大学 | Integrated preparing and forming device for magnesium alloy thin-walled pieces |
| CN105834409B (en) * | 2016-05-20 | 2017-09-19 | 河南理工大学 | A kind of magnesium alloy thin wall pieces integration system is for former |
| CN111112587A (en) * | 2019-12-30 | 2020-05-08 | 江苏奇纳新材料科技有限公司 | Method for reducing secondary shrinkage cavity of high-temperature alloy master alloy |
| CN117020157A (en) * | 2023-07-26 | 2023-11-10 | 潍坊博源动力科技有限公司 | Vibration pressurizing fine-grain casting equipment and manufacturing process |
Also Published As
| Publication number | Publication date |
|---|---|
| DE3864194D1 (en) | 1991-09-19 |
| GB2205262A (en) | 1988-12-07 |
| GB8712743D0 (en) | 1987-07-01 |
| GB2205262B (en) | 1991-03-06 |
| EP0293961B1 (en) | 1991-08-14 |
| GB8810632D0 (en) | 1988-06-08 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0293961B1 (en) | Casting method and apparatus therefor | |
| US5335711A (en) | Process and apparatus for metal casting | |
| US8136573B2 (en) | Method for production of turbine blades by centrifugal casting | |
| EP0728546B1 (en) | Directionally solidified investment casting with improved filling | |
| US11364539B2 (en) | Method and apparatus for counter-gravity mold filling | |
| US9381569B2 (en) | Vacuum or air casting using induction hot topping | |
| CN115055659B (en) | Centrifugal casting preparation method of high-temperature alloy casting | |
| US4094709A (en) | Method of forming and subsequently heat treating articles of near net shaped from powder metal | |
| US3841384A (en) | Method and apparatus for melting and casing metal | |
| US8167023B2 (en) | Apparatus for centrifugal casting under vacuum | |
| EP2144722B1 (en) | Method for production of precision castings by centrifugal casting | |
| EP0897769B1 (en) | Mold heating vacuum casting furnace | |
| EP0293960B1 (en) | Process and apparatus for metal casting | |
| CN115090850B (en) | A kind of superalloy casting centrifugal casting automatic production line and production method | |
| US6263951B1 (en) | Horizontal rotating directional solidification | |
| JP4046782B2 (en) | Method for casting melt in mold cavity, investment casting method for melt in mold cavity, and method for producing directional solidified casting | |
| CN120079854B (en) | Device and method for preparing auxiliary blade through sequential casting and ultrasonic treatment | |
| SU1037832A3 (en) | Method for making sintered products | |
| HK1196332A (en) | Vacuum or air casting using induction hot topping | |
| EP2086705B1 (en) | Method for production of turbine blades by centrifugal casting | |
| SU1048180A1 (en) | Method of preparing mould with ceramic core for casting metal for manufacturing centrifugal pump case with guide vanes |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): DE FR IT |
|
| 17P | Request for examination filed |
Effective date: 19890408 |
|
| 17Q | First examination report despatched |
Effective date: 19900412 |
|
| ITF | It: translation for a ep patent filed | ||
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR IT |
|
| REF | Corresponds to: |
Ref document number: 3864194 Country of ref document: DE Date of ref document: 19910919 |
|
| ET | Fr: translation filed | ||
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed | ||
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 19960411 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 19960424 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980130 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 19980203 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: ST |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES;WARNING: LAPSES OF ITALIAN PATENTS WITH EFFECTIVE DATE BEFORE 2007 MAY HAVE OCCURRED AT ANY TIME BEFORE 2007. THE CORRECT EFFECTIVE DATE MAY BE DIFFERENT FROM THE ONE RECORDED. Effective date: 20050506 |