EP0237318A2 - Mould for endless track type continuous casting installation - Google Patents
Mould for endless track type continuous casting installation Download PDFInfo
- Publication number
- EP0237318A2 EP0237318A2 EP87302023A EP87302023A EP0237318A2 EP 0237318 A2 EP0237318 A2 EP 0237318A2 EP 87302023 A EP87302023 A EP 87302023A EP 87302023 A EP87302023 A EP 87302023A EP 0237318 A2 EP0237318 A2 EP 0237318A2
- Authority
- EP
- European Patent Office
- Prior art keywords
- mould
- casting surface
- casting
- mould element
- slits
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Withdrawn
Links
Images
Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/10—Supplying or treating molten metal
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/06—Continuous casting of metals, i.e. casting in indefinite lengths into moulds with travelling walls, e.g. with rolls, plates, belts, caterpillars
- B22D11/0637—Accessories therefor
- B22D11/0648—Casting surfaces
- B22D11/0657—Caterpillars
Definitions
- the present invention relates to a mould for an endless track type of continuous casting installation, in which the tracks are made up of a plurality of blocks.
- this type of continuous casting installation comprises a plurality of block moulds endlessly connected to one another to define a pair of moving moulds. These moving mould pairs interact to define a mould cavity between them which is open at both ends. Molten metal is charged through a nozzle into one open end of the mould cavity and moves towards the other open end during which time it solidifies. Thus, continuous casting is carried out.
- Figure 1 shows a conventional pair of moulds b and b ⁇ used in a continuous casting installation. These define a mould cavity and each have a unitary construction comprising a bottom c and a side wall e.
- the bottom c and the side wall e have respectively a level-surface casting portion d and a side-surface casting portion f which are flat. Lugs g are clamped to maintain the moulds b and b ⁇ securely at their respective predetermined positions.
- the casting portions d and f are subjected to thermal deformations (elongation) at the high operating temperatures (for instance, 1550°C or more experienced when molten metal is charged into the mould cavity a when the continuous casting operation is started.
- the side-surface casting portions f are thus forced to curve outwardly as indicated by broken lines since the distortions are not restricted.
- a problem arises in that a gap is produced in the mould cavity a between the upper and lower moulds b and b ⁇ and molten metal leaks through the gap.
- a mould element for use in an endless tract type of continuous casting installation comprising a main casting surface on the mould element base and a side casting surface on the mould element side wall, the two casting surfaces together defining part of a mould cavity, characterised by a plurality of slits, formed in the main casting surface, extending generally in parallel with the side casting surface.
- the block includes a plurality of subblocks arranged generally in parallel with the side casting surface, the sub-blocks together defining the main casting surface.
- at least one of the opposing surfaces of adjacent sub-blocks is formed with a cut-out portion to define one or more of the slits.
- the sub-blocks may be assembled together and attached to the mould side wall by means of a tie bolt.
- elongation or expansion of the level surface casting portion caused by heating can be absorbed by the plurality of slits in the level surface so that thermal deformations can be reduced to a minimum. Furthermore, the slits can absorb shrinkage caused when the mould is cooled. Therefore, leakage of a molten metal can be prevented and design of moulds can be simplified.
- Figure 2 shows a single block or mould element 1 forming part of the end endless track mould.
- the block 1 has a base 2 having a level surface casting portion 3 and a side wall 5 having a side surface casting portion 4. These two surfaces co-operate with corresponding surfaces 3,4 on an interacting block (not shown) to define a mould cavity.
- the level surface 3 is formed with a plurality of slits 6 which extend in parallel with the side wall 5.
- each slit 6 is so selected that no molten metal flows into the slits 6 (the maximum width preferably being of the order of 0.01 - 0.1 mm) and the depth of each slit 6 is suitably selected.
- These slits 6 may be formed or machined by any suitable means e.g. by electric discharge machining or by using a knurling tool.
- the level-surface casting portion 3 of the block 1 is formed with a plurality of slits 6 in parallel with the side-surface casting portion 4 as described above, the compressive force produced by the elongation in the widthwise direction in the mould cavity of the level-surface casting portion 3 when heat can be absorbed by the slits 6. Furthermore, the tensile force produced by shrinkage of the level-surface casting portion when the block 1 is cooled can be also absorbed by the slits 6.
- thermal deformation of the side wall 5 can be reduced to a minimum so that leakage of molten metal from the mould cavity can be prevented when blocks 1 of the type described above are used.
- the provision of the slits 6 will cause not only an inflow of air but also a reduction of the contact area between the blocks 1 and the solidifying metal and therefore decrease the heat dissipation effect of the mould. Thus, heating of the mold is decreased and consequently thermal deformations can be further prevented.
- thermal deformations of the blocks 1 can be reduced, so that the design of the blocks 1 in which thermal deformations must be taken into consideration can be simplified.
- Figure 3 shows a second embodiment of a mould element 1 in accordance with the present invention.
- the side wall 5 and the base 2 are separate units and the base 2 is divided into a plurality of sub-blocks 2a, 2b, 2c and 2d which extend in parallel with the side wall 5.
- the side wall 5 and the sub-blocks 2a, 2b, 2c and 2d are assembled as a single unitary unit by means of a coupling bolt 7.
- At least one opposing surface of the sub-blocks 2a, 2b, 2c and 2d are partially cut off to define the slits 6 between the side wall 5 and the blocks 2a, 2b, 2c and 2d when they are assembled.
- the second embodiment can attain substantially the same effects and features as the first embodiment described above.
- the slits 6 may have various shape.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Continuous Casting (AREA)
- Moulds For Moulding Plastics Or The Like (AREA)
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
Abstract
Description
- The present invention relates to a mould for an endless track type of continuous casting installation, in which the tracks are made up of a plurality of blocks.
- In general, this type of continuous casting installation comprises a plurality of block moulds endlessly connected to one another to define a pair of moving moulds. These moving mould pairs interact to define a mould cavity between them which is open at both ends. Molten metal is charged through a nozzle into one open end of the mould cavity and moves towards the other open end during which time it solidifies. Thus, continuous casting is carried out.
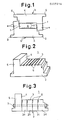
- Figure 1 shows a conventional pair of moulds b and bʹ used in a continuous casting installation. These define a mould cavity and each have a unitary construction comprising a bottom c and a side wall e. The bottom c and the side wall e have respectively a level-surface casting portion d and a side-surface casting portion f which are flat. Lugs g are clamped to maintain the moulds b and bʹ securely at their respective predetermined positions.
- In a mould of this type, the casting portions d and f are subjected to thermal deformations (elongation) at the high operating temperatures (for instance, 1550°C or more experienced when molten metal is charged into the mould cavity a when the continuous casting operation is started. The side-surface casting portions f are thus forced to curve outwardly as indicated by broken lines since the distortions are not restricted. As a result, a problem arises in that a gap is produced in the mould cavity a between the upper and lower moulds b and bʹ and molten metal leaks through the gap.
- Furthermore, when the upper and lower moulds b and bʹ cool, the casting portions d and f will shrink freely and the side walls e will curve inwardly. Thus, it is very difficult to design and construct the upper and lower moulds b and bʹ because the difference between the outward expansion when heated and the inward shrinkage when cooled must be taken into consideration.
- It is an object of the present invention to overcome the above and other problems encountered in conventional moulds used in continuous casting installations. More specifically, it is an object of the present invention to minimise thermal deformations and especially permanent deformations of the moulds caused by temperature fluctuations so that leakage of molten metal can be prevented and the design and construction of moulds can be simplified.
- According to the present invention there is provided a mould element for use in an endless tract type of continuous casting installation, comprising a main casting surface on the mould element base and a side casting surface on the mould element side wall, the two casting surfaces together defining part of a mould cavity, characterised by a plurality of slits, formed in the main casting surface, extending generally in parallel with the side casting surface.
- Preferably, the block includes a plurality of subblocks arranged generally in parallel with the side casting surface, the sub-blocks together defining the main casting surface. Preferably, at least one of the opposing surfaces of adjacent sub-blocks is formed with a cut-out portion to define one or more of the slits. The sub-blocks may be assembled together and attached to the mould side wall by means of a tie bolt.
- With a mould element according to the present invention for use in an endless track type continuous casting installation, elongation or expansion of the level surface casting portion caused by heating can be absorbed by the plurality of slits in the level surface so that thermal deformations can be reduced to a minimum. Furthermore, the slits can absorb shrinkage caused when the mould is cooled. Therefore, leakage of a molten metal can be prevented and design of moulds can be simplified.
- The invention may be carried into practice in various ways and some embodiments will be described by way of example with reference to the accompanying drawings in which:-
- Figure 1 is a schematic view illustrating the conventional arrangement of moulds in an endless track type continuous casting installation;
- Figure 2 is a perspective view of a first embodiment of a mould in accordance with the present invention; and
- Figure 3 is a view similar to Figure 2 showing a second embodiment of the present invention.
- Figure 2 shows a single block or
mould element 1 forming part of the end endless track mould. Theblock 1 has abase 2 having a levelsurface casting portion 3 and aside wall 5 having a sidesurface casting portion 4. These two surfaces co-operate withcorresponding surfaces level surface 3 is formed with a plurality ofslits 6 which extend in parallel with theside wall 5. - The maximum width of each
slit 6 is so selected that no molten metal flows into the slits 6 (the maximum width preferably being of the order of 0.01 - 0.1 mm) and the depth of eachslit 6 is suitably selected. Theseslits 6 may be formed or machined by any suitable means e.g. by electric discharge machining or by using a knurling tool. - When the level-
surface casting portion 3 of theblock 1 is formed with a plurality ofslits 6 in parallel with the side-surface casting portion 4 as described above, the compressive force produced by the elongation in the widthwise direction in the mould cavity of the level-surface casting portion 3 when heat can be absorbed by theslits 6. Furthermore, the tensile force produced by shrinkage of the level-surface casting portion when theblock 1 is cooled can be also absorbed by theslits 6. - As a result, thermal deformation of the
side wall 5 can be reduced to a minimum so that leakage of molten metal from the mould cavity can be prevented whenblocks 1 of the type described above are used. In addition, the provision of theslits 6 will cause not only an inflow of air but also a reduction of the contact area between theblocks 1 and the solidifying metal and therefore decrease the heat dissipation effect of the mould. Thus, heating of the mold is decreased and consequently thermal deformations can be further prevented. - As described above, thermal deformations of the
blocks 1 can be reduced, so that the design of theblocks 1 in which thermal deformations must be taken into consideration can be simplified. - Figure 3 shows a second embodiment of a
mould element 1 in accordance with the present invention. Theside wall 5 and thebase 2 are separate units and thebase 2 is divided into a plurality ofsub-blocks 2a, 2b, 2c and 2d which extend in parallel with theside wall 5. Theside wall 5 and thesub-blocks 2a, 2b, 2c and 2d are assembled as a single unitary unit by means of acoupling bolt 7. At least one opposing surface of thesub-blocks 2a, 2b, 2c and 2d are partially cut off to define theslits 6 between theside wall 5 and theblocks 2a, 2b, 2c and 2d when they are assembled. The second embodiment can attain substantially the same effects and features as the first embodiment described above. - It is to be understood that various variations, alternations and/or modifications may be resorted to without departing from the spirit of the present invention. For instance, the
slits 6 may have various shape.
Claims (5)
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| JP34254/86 | 1986-03-10 | ||
| JP1986034254U JPH0415402Y2 (en) | 1986-03-10 | 1986-03-10 |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP0237318A2 true EP0237318A2 (en) | 1987-09-16 |
| EP0237318A3 EP0237318A3 (en) | 1987-11-04 |
Family
ID=12409036
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP87302023A Withdrawn EP0237318A3 (en) | 1986-03-10 | 1987-03-10 | Mould for endless track type continuous casting installation |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0237318A3 (en) |
| JP (1) | JPH0415402Y2 (en) |
| KR (1) | KR870008642A (en) |
| BR (1) | BR8701088A (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0317283A1 (en) * | 1987-11-17 | 1989-05-24 | Ishikawajima-Harima Jukogyo Kabushiki Kaisha | Endless track type continuous casting machine |
| EP0369184A3 (en) * | 1988-10-19 | 1991-11-21 | Nkk Corporation | Casting machine having a travelling block mold assembly |
| WO1996033827A1 (en) * | 1995-04-24 | 1996-10-31 | Charles Christian Gerding | A continuous casting mold formed of plate elements |
| WO2011018076A1 (en) * | 2009-08-14 | 2011-02-17 | Kme Germany Ag & Co. Kg | Casting mold |
Family Cites Families (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB191501528A (en) * | 1914-05-16 | 1916-01-31 | Grenville Mellen | Method of and Apparatus for Continuous Casting. |
| CH475811A (en) * | 1967-09-07 | 1969-07-31 | Prolizenz Ag | Machine with caterpillar mold for strip casting of non-ferrous metals, especially aluminum and aluminum alloys |
| JPS5662657A (en) * | 1979-10-29 | 1981-05-28 | Mitsubishi Heavy Ind Ltd | Endless track type horizontal and continuous casting equipment |
| JPS60141354A (en) * | 1983-12-29 | 1985-07-26 | Ishikawajima Harima Heavy Ind Co Ltd | Block type continuous casting device |
-
1986
- 1986-03-10 JP JP1986034254U patent/JPH0415402Y2/ja not_active Expired
-
1987
- 1987-03-09 KR KR870002086A patent/KR870008642A/en not_active Withdrawn
- 1987-03-10 BR BR8701088A patent/BR8701088A/en unknown
- 1987-03-10 EP EP87302023A patent/EP0237318A3/en not_active Withdrawn
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| EP0317283A1 (en) * | 1987-11-17 | 1989-05-24 | Ishikawajima-Harima Jukogyo Kabushiki Kaisha | Endless track type continuous casting machine |
| EP0369184A3 (en) * | 1988-10-19 | 1991-11-21 | Nkk Corporation | Casting machine having a travelling block mold assembly |
| WO1996033827A1 (en) * | 1995-04-24 | 1996-10-31 | Charles Christian Gerding | A continuous casting mold formed of plate elements |
| US5620045A (en) * | 1995-04-24 | 1997-04-15 | Gerding; Charles C. | Continuous casting mold formed of plate elements |
| US5730206A (en) * | 1995-04-24 | 1998-03-24 | Gerding; Charles C. | Continuous strip casting mold formed of plate elements |
| WO2011018076A1 (en) * | 2009-08-14 | 2011-02-17 | Kme Germany Ag & Co. Kg | Casting mold |
| US8573284B2 (en) | 2009-08-14 | 2013-11-05 | Kme Germany Ag & Co. Kg | Casting mold |
Also Published As
| Publication number | Publication date |
|---|---|
| KR870008642A (en) | 1987-10-19 |
| BR8701088A (en) | 1987-12-29 |
| JPH0415402Y2 (en) | 1992-04-07 |
| EP0237318A3 (en) | 1987-11-04 |
| JPS62146550U (en) | 1987-09-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO1995021036A1 (en) | Mold for continuous casting and method of making the mold | |
| GB2212084A (en) | A continuous casting mould cooling arrangement | |
| US20040245684A1 (en) | Melt launder | |
| JP4109321B2 (en) | Improved continuous mold and continuous casting process | |
| RU99102238A (en) | LIQUID COOLED CRYSTALIZER | |
| US6752612B2 (en) | Mold device for injection molding of synthetic resin | |
| US3336973A (en) | Continuous casting mold | |
| JPH0415402Y2 (en) | ||
| EP0189996B1 (en) | Mould portion for use in moulding molten glass | |
| JP7105400B2 (en) | mold plate | |
| JP2683254B2 (en) | Mold equipment | |
| US2221948A (en) | Ingot positioning mold | |
| JPH0320033Y2 (en) | ||
| JP2559365B2 (en) | Endless track type | |
| JP2581982Y2 (en) | Mold | |
| KR20090008826A (en) | Mold of continuous casting mold facility | |
| KR200346874Y1 (en) | Air Vent Pin Apparatus for Rotor Die Casting | |
| CN219274386U (en) | Casting mould for continuous casting equipment | |
| JPH0373381B2 (en) | ||
| AU678696C (en) | Mold for continuous casting and method of making the mold | |
| Hargassner et al. | A Continuous Casting Mould Cooling Arrangement | |
| SU1135534A1 (en) | Metal continuous casting mould | |
| CA1275163C (en) | Endless track type continuous casting installation | |
| PT958073E (en) | PROCESS AND INSTALLATION OF CONTINUOUS LEAKING OF METALS | |
| JPS61195751A (en) | Mold block of block type continuous casting machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): DE FR GB IT |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): DE FR GB IT |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION IS DEEMED TO BE WITHDRAWN |
|
| 18D | Application deemed to be withdrawn |
Effective date: 19880505 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: TAKAHASHI, SHUZO Inventor name: FUKASE, HISAHIKO Inventor name: TSUCHIDA, YUTAKA Inventor name: MATSUI, KUNIO Inventor name: SAKO, KATSUYUKI Inventor name: NOMURA, AKIHIRO Inventor name: HASEBE, NOBUHISA |