EP0109266B1 - Computer controlled labelling machine - Google Patents
Computer controlled labelling machine Download PDFInfo
- Publication number
- EP0109266B1 EP0109266B1 EP19830306848 EP83306848A EP0109266B1 EP 0109266 B1 EP0109266 B1 EP 0109266B1 EP 19830306848 EP19830306848 EP 19830306848 EP 83306848 A EP83306848 A EP 83306848A EP 0109266 B1 EP0109266 B1 EP 0109266B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- cutter
- web
- processing means
- data processing
- master shaft
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired
Links
- 238000002372 labelling Methods 0.000 title claims description 18
- 230000003287 optical effect Effects 0.000 claims description 8
- 230000007246 mechanism Effects 0.000 description 2
- 238000004806 packaging method and process Methods 0.000 description 2
- 238000002485 combustion reaction Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 239000011521 glass Substances 0.000 description 1
- 230000003094 perturbing effect Effects 0.000 description 1
- 239000004065 semiconductor Substances 0.000 description 1
- 230000001360 synchronised effect Effects 0.000 description 1
- 230000001960 triggered effect Effects 0.000 description 1
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B26—HAND CUTTING TOOLS; CUTTING; SEVERING
- B26D—CUTTING; DETAILS COMMON TO MACHINES FOR PERFORATING, PUNCHING, CUTTING-OUT, STAMPING-OUT OR SEVERING
- B26D5/00—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting
- B26D5/20—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting with interrelated action between the cutting member and work feed
- B26D5/30—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting with interrelated action between the cutting member and work feed having the cutting member controlled by scanning a record carrier
- B26D5/32—Arrangements for operating and controlling machines or devices for cutting, cutting-out, stamping-out, punching, perforating, or severing by means other than cutting with interrelated action between the cutting member and work feed having the cutting member controlled by scanning a record carrier with the record carrier formed by the work itself
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C9/00—Details of labelling machines or apparatus
- B65C9/08—Label feeding
- B65C9/18—Label feeding from strips, e.g. from rolls
- B65C9/1865—Label feeding from strips, e.g. from rolls the labels adhering on a backing strip
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65C—LABELLING OR TAGGING MACHINES, APPARATUS, OR PROCESSES
- B65C9/00—Details of labelling machines or apparatus
- B65C9/40—Controls; Safety devices
- B65C9/42—Label feed control
- B65C9/44—Label feed control by special means responsive to marks on labels or articles
Definitions
- This invention relates to a labelling machine which is controlled by a digital data processing system. More particularly, it relates to such a system in which mechanical camming mechanisms and similar components of a conventional labelling machine are replaced by electronic controls embodied in a digital data processing system connected to control tuning, feed and related operations of a labelling machine of the type which is able to apply labels of various sizes to packaging containers of various sizes.
- labelling machines are very complex devices with many unique problems. Hitherto, it has not been known in the art to replace the mechanical control systems for main drive shafts used in labelling machines with digital data processing and electrical sensing circuits. Examples of such labelling machines are described, for example, in the following commonly assigned issued patents: U.S. 3,765,991; 4,108,709; 4,181,555; 4,188,843; 4,242,167; 4,336,095.
- GB-A-2 096 795 discloses apparatus in accordance with the prior art portion of claim 1.
- This prior document uses a sensor to sense the speed of advance of the web to enable the cutter to be operated when triggered by a signal indicative of the required cutting line on the web reaching the cutter.
- the present invention which is characterised as specified in claim 1, provides apparatus more suited to cutting comparatively small sized labels where the cutter is operable continuously and the speed of feed of the web is controlled digitally in accordance with the positions of the registration marks thereon.
- EP-A-0 074 165 is a document effective under Article 54(3) EPC which discloses a web cutting apparatus in which the speed of advance of the web is controlled by a stepping motor to cause alignment of the upper ends with the cutter. However, it does not provide the ready adjustability of the apparatus to different sized sheets as provided by the input means of the present invention.
- the stepping motor used to advance the label in the machine is directed by a program in the digital data processing means to advance the label.
- the stepper motor is directed by the program to make a predetermined number of steps per machine cycle or per container.
- the ability of the user to select any desired label length and have the machine operate properly for that length label without any mechanical adjustments to the labelling machine means that changing labels in the labelling machine is reduced from an operation taking 30 minutes or so to about 30 seconds.
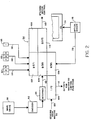
- the system 50 includes a labelling machine 52 and a digital data processing system 54.
- the digital data processing system 54 is implemented in this embodiment with a Gould Modicon-P190/484, although it should be understood that the digital data processing system 54 could be implemented with any one of a large number of commercially available control oriented data processing systems which, for example, utilize commercially available microprocessor integrated circuits, such as an Intel 8086, Intel 8088, Motorola 68000, Fairchild 9445, National Semiconductor 16000, or the like, to form the processing unit of such control oriented data processing systems.
- microprocessor integrated circuits such as an Intel 8086, Intel 8088, Motorola 68000, Fairchild 9445, National Semiconductor 16000, or the like, to form the processing unit of such control oriented data processing systems.
- the labelling machine 52 includes a cutter 56 having a shaft 58 including a mark 60, which is sensed by an encoder 62, which supplies shaft 58 position and rotation rate data signals as inputs to the digital data processing system 54 on line 63, through an interface 65.
- the encoder 62 could be replaced with any suitable sensor, such as a magnetic sensing means, with a structure of the shaft 58 serving the function of the mark 60 by perturbing a magnetic field to which the magnetic sensing means is responsive.
- the encoder 62 is preferably implemented with a C and A Model HT-11B encoder, obtainable from C and A Products.
- the interface 65 is preferably implemented with a PCEF Encoder Interface Module, which converts the shaft 58 position and rate information to binary coded decimal (BCD) form.
- the digital data processing system 54 supplies a rotation rate control signal at a rate of, for example, 2,000 pulses per revolution of a label- feed roll 66 on line 64 to a stepping motor 67, which is connected to feed roll 66 by a shaft 69, through a stepping motor control 71.
- the rotation rate control signal on line 64 is such that the feed roll 66 will supply continuous label sheet 68 to the cutter at a proper rate so that the cutter 56 will separate an individual label 70 from the sheet 68 at the kerf 72 dividing each individual label from its next adjacent neighbors.
- Each label 70 includes a positioning mark 74.
- the positioning mark 74 is sensed by an optical sensor 76 as a means of preventing the sheet 68 from “creeping" with respect to the cutter 56, so that the cutter 56 begins to slit the sheet 68 at other locations than the kerf 72.
- the optical sensor 76 is connected to the data processing system 54 by line 78.
- the optical sensor 76 supplies a signal on line 78 when a mark 74 is sensed.
- the digital data processing system 54 compares the shaft 58 at the time the mark 74 is sensed with the position shaft 58 should have in order for label 70 feed and shaft 58 position to be synchronized for proper label 70 slitting.
- the optical sensor 76 is preferably implemented with a Banner CVG-1 sensor, obtainable from Banner, Inc., Minneapolis, Minnesota.
- the length of the new labels in inches is entered into the digital data processing system 54 by means of thumbwheel switches 82 on the front panel 84.
- An angular position in degrees for shaft 58 when a mark 74 should be sensed by sensor 76 is dialed in with thumbwheel switches 83.
- a tolerance for the angular position in degrees is also entered by means of thumbwheel switch 85.
- FIG 2 shows the data processing system 54 in the system of Figure 1 in more detail.
- the system 54 includes a processor 100 and input modules 102,104, and 106 are connected to supply input to the processor 100.
- An input/ output module 108 is also connected to supply inputs to the processor 100 and supply outputs from the system 54 on line 112 for certain machine control functions conventional in the art and not forming a part of this invention. However, these other control functions are provided using the same data processing system 54 used for the rest of the invention.
- An output module 110 is connected to receive outputs from the processor 100, to be supplied to the stepper motor control on line 113.
- Interface module 65 is connected to the input module 104 of data processing system 54 by line 63.
- the thumbwheel switches 82, 83, and 85 are respectively connected to the input multiplexer module 102 by lines 114, 116, and 118.
- Inputs from other sensors attached to the labelling machine 52 are supplied on line 120 to the I/0 module 108.
- Outputs for labelling machine 52 control functions are supplied by the I/0 module 108 on line 112.
- Optical sensor 76 supplies the input signal to input module 106 on line 78 when it senses the presence of a registration mark 74.
- the system 50 feeds labels 70 from roll 80 on a continuous basis to the cutter 56 in such a manner that the cutter will cut the labels 70 at the kerf 72 and supply the cut labels 70 to a container in a consistent manner.
- Changing the label machine 52 to accommodate different size labels is a simple matter of entering the new label length into the digital data processing system 54.
- the mark 74 can be placed on any desired location on the label.
Landscapes
- Life Sciences & Earth Sciences (AREA)
- Forests & Forestry (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Labeling Devices (AREA)
Description
- This invention relates to a labelling machine which is controlled by a digital data processing system. More particularly, it relates to such a system in which mechanical camming mechanisms and similar components of a conventional labelling machine are replaced by electronic controls embodied in a digital data processing system connected to control tuning, feed and related operations of a labelling machine of the type which is able to apply labels of various sizes to packaging containers of various sizes.
- In conventional machines used to apply different size labels to different size cans, glass bottles, boxes or other packaging containers, timing marks, cams, gears and similar interconnected mechanical elements are employed to assure that the containers and labels are supplied to the machine in an orderly fashion and synchronously with respect to each other so that a single label is uniformly placed in a desired location on the container. Some control functions of labelling machines have also been implemented with digital circuits, including microprocessors.
- It is also known_ in the prior art to replace various mechanical timing devices-in complex machines, such as internal combustion engines with digital electronics. Many such timing mechanisms have been replaced in automobile engines through the use of digital data processing circuits embodied in microprocessor integrated circuits, in combination with various electronic and electromechanical sensing circuits.
- However, labelling machines are very complex devices with many unique problems. Hitherto, it has not been known in the art to replace the mechanical control systems for main drive shafts used in labelling machines with digital data processing and electrical sensing circuits. Examples of such labelling machines are described, for example, in the following commonly assigned issued patents: U.S. 3,765,991; 4,108,709; 4,181,555; 4,188,843; 4,242,167; 4,336,095.
- Accordingly, it is an object of this invention to adapt digital data processing technology to a labelling machine.
- It is another object of the invention to provide a digital data processing system in which electrical circuits are utilized to provide inputs representing positions and other information about the various components of a labelling machine and the labels and containers passing through the machine.
- GB-A-2 096 795 discloses apparatus in accordance with the prior art portion of
claim 1. This prior document uses a sensor to sense the speed of advance of the web to enable the cutter to be operated when triggered by a signal indicative of the required cutting line on the web reaching the cutter. As compared therewith the present invention, which is characterised as specified inclaim 1, provides apparatus more suited to cutting comparatively small sized labels where the cutter is operable continuously and the speed of feed of the web is controlled digitally in accordance with the positions of the registration marks thereon. - EP-A-0 074 165 is a document effective under Article 54(3) EPC which discloses a web cutting apparatus in which the speed of advance of the web is controlled by a stepping motor to cause alignment of the upper ends with the cutter. However, it does not provide the ready adjustability of the apparatus to different sized sheets as provided by the input means of the present invention.
- In the preferred form of the invention, the stepping motor used to advance the label in the machine is directed by a program in the digital data processing means to advance the label. The stepper motor is directed by the program to make a predetermined number of steps per machine cycle or per container.
- The ability of the user to select any desired label length and have the machine operate properly for that length label without any mechanical adjustments to the labelling machine means that changing labels in the labelling machine is reduced from an operation taking 30 minutes or so to about 30 seconds.
- The invention should be more readily apparent to those skilled in the art, after review of the following more detailed description of the invention, taken together with the accompanying drawings, in which:
- Figure 1 is a block diagram of a computer controlled labelling machine in accordance with the invention.
- Figure 2 is a plan view of a portion of the system shown in Figure 1.
- Turning now to the drawings, more particularly to Figure 1, there is shown a
system 50 in accordance with the invention. Thesystem 50 includes alabelling machine 52 and a digitaldata processing system 54. The digitaldata processing system 54 is implemented in this embodiment with a Gould Modicon-P190/484, although it should be understood that the digitaldata processing system 54 could be implemented with any one of a large number of commercially available control oriented data processing systems which, for example, utilize commercially available microprocessor integrated circuits, such as an Intel 8086, Intel 8088, Motorola 68000, Fairchild 9445, National Semiconductor 16000, or the like, to form the processing unit of such control oriented data processing systems. - The
labelling machine 52 includes acutter 56 having ashaft 58 including amark 60, which is sensed by anencoder 62, which suppliesshaft 58 position and rotation rate data signals as inputs to the digitaldata processing system 54 online 63, through aninterface 65. Theencoder 62 could be replaced with any suitable sensor, such as a magnetic sensing means, with a structure of theshaft 58 serving the function of themark 60 by perturbing a magnetic field to which the magnetic sensing means is responsive. In practice, theencoder 62 is preferably implemented with a C and A Model HT-11B encoder, obtainable from C and A Products. Theinterface 65 is preferably implemented with a PCEF Encoder Interface Module, which converts theshaft 58 position and rate information to binary coded decimal (BCD) form. The digitaldata processing system 54 supplies a rotation rate control signal at a rate of, for example, 2,000 pulses per revolution of a label-feed roll 66 on line 64 to astepping motor 67, which is connected to feedroll 66 by ashaft 69, through a steppingmotor control 71. The rotation rate control signal on line 64 is such that thefeed roll 66 will supplycontinuous label sheet 68 to the cutter at a proper rate so that thecutter 56 will separate anindividual label 70 from thesheet 68 at thekerf 72 dividing each individual label from its next adjacent neighbors. - Each
label 70 includes apositioning mark 74. Thepositioning mark 74 is sensed by anoptical sensor 76 as a means of preventing thesheet 68 from "creeping" with respect to thecutter 56, so that thecutter 56 begins to slit thesheet 68 at other locations than thekerf 72. Theoptical sensor 76 is connected to thedata processing system 54 byline 78. Theoptical sensor 76 supplies a signal online 78 when amark 74 is sensed. The digitaldata processing system 54 compares theshaft 58 at the time themark 74 is sensed with theposition shaft 58 should have in order forlabel 70 feed andshaft 58 position to be synchronized forproper label 70 slitting. Theoptical sensor 76 is preferably implemented with a Banner CVG-1 sensor, obtainable from Banner, Inc., Minneapolis, Minnesota. - When it is desired to replace a
roll 80 of thelabels 70 with a roll of labels having a different length than that of thelabels 70, the length of the new labels in inches is entered into the digitaldata processing system 54 by means ofthumbwheel switches 82 on thefront panel 84. An angular position in degrees forshaft 58 when amark 74 should be sensed bysensor 76 is dialed in withthumbwheel switches 83. A tolerance for the angular position in degrees is also entered by means ofthumbwheel switch 85. - Figure 2 shows the
data processing system 54 in the system of Figure 1 in more detail. - The
system 54 includes aprocessor 100 and input modules 102,104, and 106 are connected to supply input to theprocessor 100. An input/output module 108 is also connected to supply inputs to theprocessor 100 and supply outputs from thesystem 54 online 112 for certain machine control functions conventional in the art and not forming a part of this invention. However, these other control functions are provided using the samedata processing system 54 used for the rest of the invention. Anoutput module 110 is connected to receive outputs from theprocessor 100, to be supplied to the stepper motor control online 113. -
Interface module 65 is connected to theinput module 104 ofdata processing system 54 byline 63. The thumbwheel switches 82, 83, and 85 are respectively connected to theinput multiplexer module 102 bylines line 120 to the I/0module 108. Outputs forlabelling machine 52 control functions are supplied by the I/0module 108 online 112.Optical sensor 76 supplies the input signal to inputmodule 106 online 78 when it senses the presence of aregistration mark 74. - The
system 50 feeds labels 70 fromroll 80 on a continuous basis to thecutter 56 in such a manner that the cutter will cut thelabels 70 at thekerf 72 and supply thecut labels 70 to a container in a consistent manner. Changing thelabel machine 52 to accommodate different size labels is a simple matter of entering the new label length into the digitaldata processing system 54. - It should further be apparent to those skilled in the art that various changes in form and detail of the invention as shown and described may be made. For example, the
mark 74 can be placed on any desired location on the label.
Claims (2)
Applications Claiming Priority (4)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US441040 | 1982-11-12 | ||
| US06/441,040 US4519868A (en) | 1982-11-12 | 1982-11-12 | Computer controlled labelling machine |
| US532783 | 1983-09-16 | ||
| US06/532,783 US4552608A (en) | 1983-09-16 | 1983-09-16 | System for computer controlled labeling machine |
Publications (4)
| Publication Number | Publication Date |
|---|---|
| EP0109266A2 EP0109266A2 (en) | 1984-05-23 |
| EP0109266A3 EP0109266A3 (en) | 1985-05-15 |
| EP0109266B1 true EP0109266B1 (en) | 1988-04-27 |
| EP0109266B2 EP0109266B2 (en) | 1996-11-27 |
Family
ID=27032650
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19830306848 Expired - Lifetime EP0109266B2 (en) | 1982-11-12 | 1983-11-09 | Computer controlled labelling machine |
Country Status (4)
| Country | Link |
|---|---|
| EP (1) | EP0109266B2 (en) |
| JP (1) | JP2527825Y2 (en) |
| AU (1) | AU2110883A (en) |
| DE (1) | DE3376411D1 (en) |
Families Citing this family (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| GB2189226A (en) * | 1986-04-18 | 1987-10-21 | Portals Eng Ltd | Label splicing machine |
| GB8711402D0 (en) * | 1987-05-14 | 1987-06-17 | Portals Eng Ltd | Article labelling apparatus |
| DE3824090A1 (en) * | 1988-07-15 | 1990-02-15 | Schips Ag | LABEL DISPENSER |
| EP0370642A1 (en) * | 1988-11-01 | 1990-05-30 | John Waddington PLC | Improvements relating to the application of labels to articles |
| DE3918665A1 (en) * | 1989-06-08 | 1990-12-13 | Bhs Bayerische Berg | METHOD AND DEVICE FOR CONTROLLING A FORMAT LENGTH CUTTING OF MATERIALS |
| US5022950A (en) * | 1989-07-17 | 1991-06-11 | Philip Morris Incorporated | On-line embossing apparatus for a labeling machine |
| CA2114204A1 (en) * | 1993-02-23 | 1994-08-24 | Charles Robert Mason | Batter-like coating |
| US5821724A (en) * | 1995-02-03 | 1998-10-13 | Cms Gilbreth Packaging Systems | Feedback limiter for closed loop motor controller |
| AU669431B2 (en) * | 1993-06-17 | 1996-06-06 | Cms Gilbreth Packaging Systems, Inc. | Registration system for web feeding |
| US5478422A (en) * | 1993-09-16 | 1995-12-26 | B & H Manufacturing Company, Inc. | Computer controlled turret type labeling machine |
| US5858143A (en) * | 1993-09-16 | 1999-01-12 | B & H Manufacturing, Inc. | Computer controlled labeling machine for applying labels including stretch labels and tactilely sensible indicia on articles |
| US5853117A (en) * | 1995-10-31 | 1998-12-29 | Moore Business Forms, Inc. | Separator for linerless labels |
| GB0114834D0 (en) * | 2001-06-18 | 2001-08-08 | Statefresh Ltd | A method of and apparatus for affixing backing to plates |
Family Cites Families (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US4239570A (en) * | 1978-10-10 | 1980-12-16 | The Meyercord Co. | Method and machine for transferring indicia to tapered articles |
| EP0011967A1 (en) * | 1978-11-28 | 1980-06-11 | Harland Machine Systems Limited | Labelling machines |
| JPS571045A (en) * | 1980-05-26 | 1982-01-06 | Tokyo Electric Co Ltd | Controller for label feed |
| US4384500A (en) * | 1980-11-20 | 1983-05-24 | Owens-Illinois, Inc. | Registration control for a label cutoff apparatus |
| US4415978A (en) * | 1981-04-14 | 1983-11-15 | Molins Machine Company, Inc. | Cut-to-mark cut-off control automated for splice and order change |
| EP0074165A1 (en) * | 1981-07-16 | 1983-03-16 | Trebor Limited | Separation system for continuous wrapping material |
-
1983
- 1983-11-09 EP EP19830306848 patent/EP0109266B2/en not_active Expired - Lifetime
- 1983-11-09 DE DE8383306848T patent/DE3376411D1/en not_active Expired
- 1983-11-09 AU AU21108/83A patent/AU2110883A/en not_active Abandoned
-
1994
- 1994-03-22 JP JP1994003757U patent/JP2527825Y2/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| EP0109266A3 (en) | 1985-05-15 |
| EP0109266B2 (en) | 1996-11-27 |
| JP2527825Y2 (en) | 1997-03-05 |
| AU2110883A (en) | 1984-05-17 |
| JPH0744500U (en) | 1995-11-21 |
| DE3376411D1 (en) | 1988-06-01 |
| EP0109266A2 (en) | 1984-05-23 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US4519868A (en) | Computer controlled labelling machine | |
| US4552608A (en) | System for computer controlled labeling machine | |
| EP0109266B2 (en) | Computer controlled labelling machine | |
| US6641684B2 (en) | Method of and apparatus for producing labels | |
| US4955265A (en) | Web cutting position control system | |
| EP0296290B1 (en) | Product-out-of-registration control for high speed wrapping machine | |
| US5413651A (en) | Universal roll-fed label cutter | |
| EP0180401B1 (en) | Document inserter systems | |
| CA1168631A (en) | Labeling machine | |
| US5608639A (en) | System and method for printing, assembly and verifying a multiple-part printed product | |
| EP1468913B1 (en) | Machine for sealing containers by applying a covering film | |
| CA1124817A (en) | Electronic program control | |
| US4726865A (en) | Limp label application process | |
| GB2289664A (en) | Manufacture of labels | |
| US4221144A (en) | Paper feed control for automatic photographic paper cutter | |
| EP0409531A3 (en) | On-line embossing apparatus for a labeling machine | |
| GB2048830A (en) | Automatic machine for sorting items of correspondence into batches each having a different general destination | |
| US3029675A (en) | Device for severing continuously moving strip at predetermined locations | |
| US4715846A (en) | Trailing panel folder | |
| GB2197731A (en) | Wrapping machine control | |
| US3253544A (en) | Manufacture and use of labels for bottles, containers, and the like | |
| US4495584A (en) | Intermittent driving system for synchronizing control of conveyor and dispensing systems | |
| NL1007637C2 (en) | Printing and finishing of documents. | |
| EP0074165A1 (en) | Separation system for continuous wrapping material | |
| JP2664709B2 (en) | Packing system |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB IT |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Designated state(s): DE FR GB IT |
|
| 17P | Request for examination filed |
Effective date: 19851107 |
|
| 17Q | First examination report despatched |
Effective date: 19860603 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): DE FR GB IT |
|
| ITF | It: translation for a ep patent filed | ||
| REF | Corresponds to: |
Ref document number: 3376411 Country of ref document: DE Date of ref document: 19880601 |
|
| ET | Fr: translation filed | ||
| PLBI | Opposition filed |
Free format text: ORIGINAL CODE: 0009260 |
|
| 26 | Opposition filed |
Opponent name: KRONES AG HERMANN KRONSEDER MASCHINENFABRIK Effective date: 19890126 |
|
| PLAB | Opposition data, opponent's data or that of the opponent's representative modified |
Free format text: ORIGINAL CODE: 0009299OPPO |
|
| R26 | Opposition filed (corrected) |
Opponent name: KRONES AG HERMANN KRONSEDER MASCHINENFABRIK, Effective date: 19890126 |
|
| ITTA | It: last paid annual fee | ||
| PLAW | Interlocutory decision in opposition |
Free format text: ORIGINAL CODE: EPIDOS IDOP |
|
| PUAH | Patent maintained in amended form |
Free format text: ORIGINAL CODE: 0009272 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: PATENT MAINTAINED AS AMENDED |
|
| 27A | Patent maintained in amended form |
Effective date: 19961127 |
|
| AK | Designated contracting states |
Kind code of ref document: B2 Designated state(s): DE FR GB IT |
|
| ITF | It: translation for a ep patent filed | ||
| APAC | Appeal dossier modified |
Free format text: ORIGINAL CODE: EPIDOS NOAPO |
|
| APAC | Appeal dossier modified |
Free format text: ORIGINAL CODE: EPIDOS NOAPO |
|
| ET | Fr: translation filed | ||
| ET3 | Fr: translation filed ** decision concerning opposition |
Free format text: CORRECTIONS |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: IF02 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20021106 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20021108 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20021114 Year of fee payment: 20 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20031108 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 |
|
| APAH | Appeal reference modified |
Free format text: ORIGINAL CODE: EPIDOSCREFNO |