SUMMERY OF THE UTILITY MODEL
The utility model provides an automatic welding centering device applied to tank body, pipeline butt welding or longitudinal welding equipment, aiming at solving the defects in the prior art.
In order to achieve the above purpose, the technical scheme adopted by the utility model is as follows:
an automatic welding centering device comprises a bracket, a sliding block, a movable guide rail, a cross sliding table, a welding gun and a laser range finder; the front end of the bracket is connected with the cross sliding table, the rear end of the bracket is fixedly connected with the sliding block, and the sliding block can move on the movable guide rail; the cross sliding table is fixed to the welding gun through a connecting rod assembly, the laser range finder is fixed to correspond to the connecting rod assembly on the side edge of the welding gun, and the laser range finder is used for detecting the vertical height of a welding workpiece below the welding gun and the distance of the edge of a welding seam between the welding workpieces.
According to a preferable technical scheme, the connecting rod assembly comprises a first connecting rod perpendicular to the cross sliding table and a second connecting rod arranged at the free end of the first connecting rod and perpendicular to the first connecting rod; the end of the second connecting rod, which is deviated from the first connecting rod, clamps the welding gun through a clamp.
Further, the clamp is a clamping structure with an adjustable angle.
According to a preferred technical scheme, the laser range finder is fixedly connected to the clamp through a range finder support.
In another preferred technical scheme, the cross sliding table comprises a Y-direction sliding table fixedly connected with the bracket and an X-direction sliding table fixed in front of the Y-direction sliding table; a Y-direction guide rail is arranged on the front side of the Y-direction sliding table, and the X-direction sliding table can move on the Y-direction guide rail in the Y-direction through a sliding block; the X-direction sliding table is arranged on the front side of the X-direction sliding table, and the connecting rod assembly is connected to the X-direction guide rail through a sliding block and can move on the X-direction guide rail in the X-direction.
Furthermore, the X-direction guide rail and the Y-direction guide rail are both of a screw rod structure, and the sliding block is a screw rod nut; the X-direction guide rail is driven by an X-direction motor arranged on the side edge of the X-direction sliding table, and the Y-direction guide rail is driven by a Y-direction motor arranged on the side edge of the Y-direction sliding table.
Furthermore, the rear end of the bracket is fixedly connected with the sliding block through a bottom plate perpendicular to the bracket.
According to the second aspect of the utility model, the utility model discloses an automatic welding gun centering system which comprises the automatic welding gun centering device.
A welding gun automatic centering system applying the device comprises
The laser ranging module is used for detecting the vertical height of a welding workpiece below the welding gun and the distance of the welding seam edge between the welding workpieces;
the welding cooperative control module is used for determining the height distance between a welding gun head of the welding gun and a welding seam according to the vertical height of a welding workpiece; the welding line swing center position is determined according to the distance of the welding line edges between the welding workpieces; and
the cross sliding table adjusting module is used for adjusting the X-direction horizontal position and the Y-direction vertical position of the welding gun according to the measurement parameters; and the deviation between the welding gun head and the middle point position of the oscillation amplitude of the welding seam is compensated by the swinging of the X-direction sliding table, and the height distance between the welding gun head and the welding seam is adjusted by the Y-direction sliding table.
The utility model has the beneficial effects that:
the automatic centering device of the welding gun is used as a compensation device for adjusting the height and the swing amplitude of the welding gun in the welding process. In the welding process, the swing amplitude of the welding gun is preset, and the swing amplitude can completely cover the welding seam; the centering device is used for measuring horizontal distance and vertical distance by using laser ranging, and can be used for offsetting if a welding seam deviates from a preset track. The distance measuring method is direct and simple, and real-time adjustment can be realized.
The device of the utility model uses the cross sliding table as a welding deviation adjusting mechanism to integrally move the welding swing to cover the position to be welded so as to prevent the welding deviation phenomenon.
The device also expands the application range of the welding equipment. The welding gun automatic centering device can realize the welding of the pipe (tank) in the diameter direction and the axial direction, can also weld the plane linear welding of plates and the welding of a prefabricated curve track, and has wide application and high practicability.
Detailed Description
The common welding scene is that a welding gun is fixed, an excircle is welded by rolling a tank body or the tank body is horizontally welded by translating, common automatic welding equipment is adopted, the problems of welding deviation and the like can occur under the condition that the position of the welding gun is kept unchanged due to the fact that butt joint of base materials at a welding seam is not uniform, errors exist in base material processing, or other uncertain factors exist in the welding process, and the position deviation is generated randomly, cannot be pre-judged, is not controlled, cannot be treated in real time, and cannot meet the requirements of the production process. According to the utility model, the laser range finder and the welding gun are synchronized, the range data is fed back in real time, and the left and right swing amplitude of the welding gun is adjusted, so that the welding seam can completely cover the preset welding seam.
The following describes a specific embodiment of a schematic structural diagram of an automatic centering system for a welding gun according to the present invention with reference to an embodiment. The following examples are only used to illustrate the technical solutions of the present invention more clearly, and the protection scope of the present invention is not limited thereby; various changes and modifications can be made by one skilled in the art without departing from the spirit and scope of the utility model, and all equivalent technical solutions also fall within the scope of the utility model, which is defined by the claims.
Example 1
Fig. 1 shows a schematic structural view of embodiment 1 of the automatic centering device for a welding gun according to the present invention.
The automatic welding gun centering device comprises a support 1, a sliding block 2, a movable guide rail 3, a cross sliding table 4, a welding gun 5 and a laser range finder 6; the front end of the bracket 1 is connected with the cross sliding table 4, the rear end of the bracket 1 is fixedly connected with the sliding block 2, and the sliding block 2 can move on the movable guide rail 3; the cross sliding table 4 is fixed through a connecting rod assembly, the welding gun 5 is fixed, the laser range finder 6 is fixed on the connecting rod assembly corresponding to the side edge of the welding gun 5, and the laser range finder 6 is used for detecting the vertical height of a welding workpiece below the welding gun 5 and the distance of the welding seam edge between the welding workpieces.
The laser range finder of the device measures the distance between the welding edges of two welding parent metals, determines the middle point of the swing of the welding seam, and measures parameters for adjusting the X-direction horizontal position and the Y-direction vertical position of a welding gun through a cross sliding table: the value measured by the X-direction horizontal position is compensated by the X-direction swing, and the value measured by the Y-direction vertical position is used for adjusting the distance between the welding gun and the workpiece in the Y direction, so that the centering of the welding gun head is realized.
Example 2
On the basis of the embodiment 1, the automatic welding gun centering device is improved in the following way.
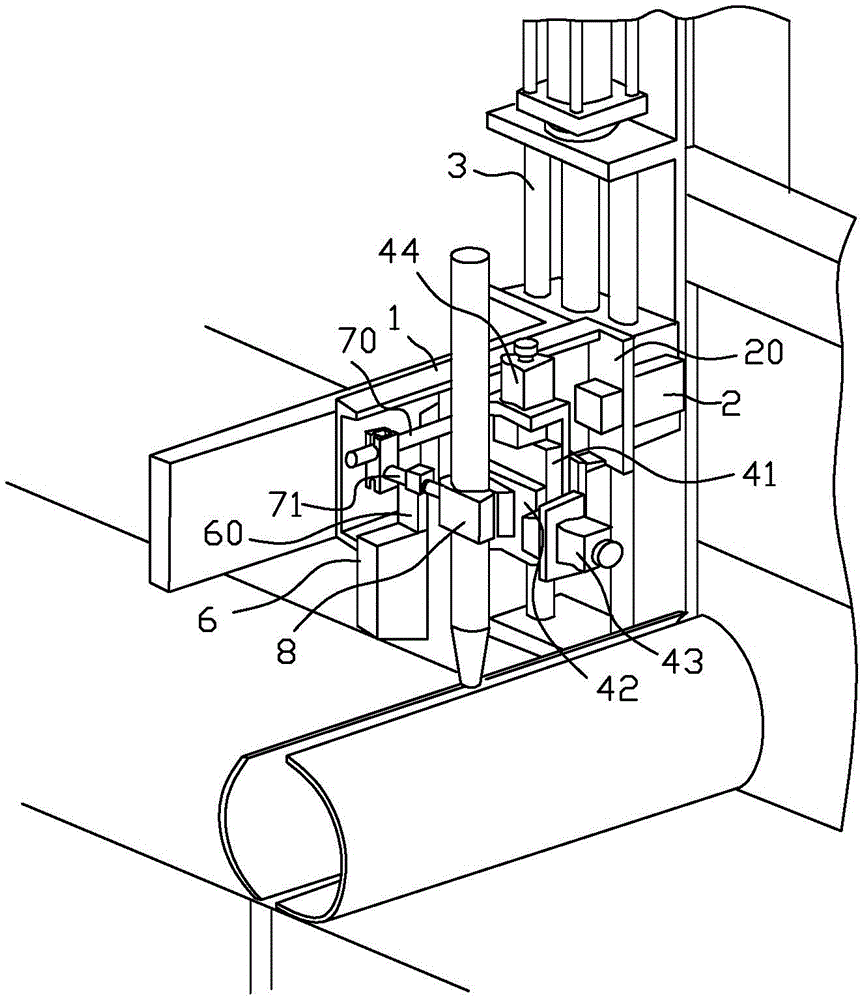
As shown in fig. 2, the connecting rod assembly comprises a first connecting rod 70 perpendicular to the cross sliding table 4 and a second connecting rod 71 arranged at the free end of the first connecting rod 70 and perpendicular to the first connecting rod 70; the second link 71 is biased away from the end of the first link 70 to hold the welding gun 5 by a clamp 8. And the welding gun 5 is fixedly connected with the connecting rod assembly after being installed and moves along with the sliding block of the cross sliding table.
The clamp 8 is a clamping structure with an adjustable angle, and the structure can adopt an angle adjusting mechanism or a full-automatic joint to connect the clamp 8 and the second connecting rod 71 in practical application, so that the welding angle of the welding gun can be adjusted along with the welding requirement.
The laser range finder 6 is fixedly connected to the fixture through a range finder support 60, so that the laser range finder and a welding gun can move synchronously in the welding process.
The rear end of the bracket 1 is fixedly connected with the sliding block 2 through a bottom plate 20 vertical to the bracket.
As shown in fig. 3, the cross sliding table 4 comprises a Y-direction sliding table 41 fixedly connected with the bracket 1 and an X-direction sliding table 42 fixed in front of the Y-direction sliding table 41; a Y-direction guide rail is arranged on the front side of the Y-direction sliding table 41, and the X-direction sliding table 42 can move on the Y-direction guide rail in the Y-direction through a sliding block; the front side of the X-direction sliding table 42 is provided with a connecting rod assembly which is connected to the X-direction guide rail through a sliding block and can move on the X-direction guide rail in the X-axis direction.
The X-direction guide rail and the Y-direction guide rail are both of screw rod structures, and the sliding block is a screw rod nut; the X-direction guide rail is driven by an X-direction motor 43 provided on the side of the X-direction slide table 42, and the Y-direction guide rail is driven by a Y-direction motor 44 provided on the side of the Y-direction slide table 41.
The cross sliding table is controlled by a servo motor, and horizontal and vertical movement is realized by controlling the motor through X, Y; the specific control operation of the servo control system is realized according to the structure of the application, and the software setting of the system is the routine operation of the technicians in the field.
Example 3
This example shows an automatic centering system for a welding gun using the apparatus of the above example 1 or 2, as shown in fig. 4, the system comprising
The laser ranging module is used for detecting the vertical height of a welding workpiece below the welding gun and the distance of the welding seam edge between the welding workpieces;
the welding cooperative control module is used for determining the height distance between a welding gun head of the welding gun and a welding seam according to the vertical height of a welding workpiece; the welding line swing center position is determined according to the distance of the welding line edges between the welding workpieces; and
the cross sliding table adjusting module is used for adjusting the X-direction horizontal position and the Y-direction vertical position of the welding gun according to the measurement parameters; and the deviation between the welding gun head and the middle point position of the oscillation amplitude of the welding seam is compensated by the swinging of the X-direction sliding table, and the height distance between the welding gun head and the welding seam is adjusted by the Y-direction sliding table.
The automatic welding gun centering device and the automatic welding gun centering system are used as a device for adjusting and compensating the height and the swing amplitude of the welding gun in the welding process; in the welding process, the swing amplitude of the welding gun is preset, and the swing amplitude can completely cover the welding seam. The centering device has the function that if the welding seam deviates from the preset track, the centering device can be used for offsetting; fig. 5 shows a work flow diagram of the system, including the following adjustment methods:
1. the laser range finder measures the vertical distance of the welding workpiece, and the welding cooperative controller judges whether the height between the welding gun and the welding workpiece is at the optimal position according to the measurement parameters; if not, the slide block is driven to move through the Y-direction motor, and the height of the welding gun and the workpiece is adjusted to the optimal position;
2. the laser range finder measures the distance between the horizontal butt welding workpieces of the welding workpieces, and the welding cooperation controller judges whether the welding gun is in the center position of a welding seam between the butt welding workpieces according to the measurement parameters; if not, the sliding block is driven to move through the X-direction motor, the distance between the horizontal butt welding workpieces covered by the swing center position of the welding gun is adjusted, and the welding deviation phenomenon of a welding seam is reduced;
3. the system can perform centering adjustment and welding aiming at different welding workpieces in the specific operation process, and specifically comprises the following conditions:
(1) under the control of the laser range finder measuring instrument and the cross sliding table, when the pipeline moves along the axis direction, the pipeline is transversely welded;
(2) under the control of the laser range finder measuring instrument and the cross sliding table, the welding of the outer circle of the pipeline is realized when the pipeline rolls;
(3) under the control of the laser range finder measuring instrument and the cross sliding table, when the sheet material horizontally moves, the sheet material is in straight line butt welding;
(4) and under the control of the laser range finder measuring instrument and the cross sliding table, the sheet material curve is in butt joint welding when the sheet material with the preset track moves horizontally.
The laser measurement is more direct in the embodiment, the diameter direction adjustment and the axial adjustment of the pipe (tank) welding can be adjusted, the welding deviation is prevented, and the real-time adjustment can be realized; the welding gun automatic centering device can realize the welding of the pipe (tank) in the diameter direction and the axial direction, and can also realize the plane linear welding and the prefabricated curve track welding of the welding plate.