SUMMERY OF THE UTILITY MODEL
The utility model discloses aim at solving one of the technical problem that exists among the prior art at least. Therefore, the utility model provides a top is cut and is detected carrier band packagine machine can realize detecting, blank, packing by the complete machine, need not manual work, production efficiency is high, guarantees that product quality is stable.
According to the utility model discloses a top is cut and is detected carrier band packagine machine of first aspect embodiment, include:
the multi-station turntable transferring device comprises a first driving device, a multi-station turntable, a plurality of material taking mechanisms, a turntable fixing frame and a second driving device, wherein the multi-station turntable is movably arranged below the turntable fixing frame, the material taking mechanisms are arranged at stations of the multi-station turntable, the first driving device is used for driving the multi-station turntable to rotate, and the second driving device is used for driving the material taking mechanisms to take materials;
the carrier band heat-seal packaging module is arranged on one side of the multi-station turntable transfer device and comprises a carrier band guide rail, a feeding mechanism and a heat-seal mechanism, the carrier band guide rail comprises a ratchet wheel and a third driving device, the ratchet wheel is arranged at one end in the carrier band guide rail, the third driving device is used for driving the ratchet wheel to drive the carrier band to move, the feeding mechanism is arranged above the carrier band guide rail, and the heat-seal mechanism is arranged between the feeding mechanism and the carrier band guide rail;
the CCD detection device is arranged at the outer side of the multi-station turntable transfer device and is used for detecting products;
the CID detection device is arranged on the outer side of the multi-station turntable transfer device and is used for detecting the flatness of the product;
the top cutting device is arranged on the outer side of the multi-station turntable transfer device and is positioned between the CCD detection device and the CID detection device, and the top cutting device is used for cutting off a product from a material belt;
and the positioning guide device is arranged between the CID detection device and the top cutting device and is used for changing the direction of the product.
According to the utility model discloses top is cut and is detected carrier band packagine machine has following beneficial effect at least: the material belt sequentially passes through a CCD detection device and a top cutting device, after the CCD detection device detects products on the material belt, the top cutting device cuts the detected products off the material belt, a multi-station turntable transfer device transfers the products from the top cutting device to a positioning guide device, after the positioning guide device guides the product position, the multi-station turntable transfer device transfers the guided products to a CID detection device for flatness detection, finally, a plurality of public position turntable transfer devices transfer the qualified products to a carrier belt of a carrier belt heat-seal packaging module, and the carrier belt heat-seal packaging module heat-seals and packages the products on the carrier belt; under the effect that the multistation carousel moved the device, steps such as above-mentioned CCD detects, top is cut, the position is led just, CID detects, carrier band packing can be gone on simultaneously, need not artifical supplementary, and production efficiency is high to the product can carry out comprehensive CCD and detect with CID, guarantees product quality, and the setting of carousel formula simultaneously can reduce the complete machine volume, saves space.
According to some embodiments of the present invention, the top-cut detection carrier tape packaging machine further comprises a stepping pulling device, wherein the stepping pulling device and the CCD detection device are respectively disposed on two sides of the top-cut device, and the feeding side and the discharging side of each device are all on the same straight line; the stepping material pulling device comprises a material pulling frame, a fourth driving device, a fifth driving device, a rod lifting mechanism, a bottom roller and a pressure adjusting rod; the bottom rollers are rotatably arranged between the material pulling frames, and the fourth driving device is used for driving the bottom rollers to rotate; the middle part of the rod lifting mechanism is movably connected with the inner walls of the two sides of the material pulling frame, the rod lifting mechanism is positioned above the bottom roller, the rod lifting mechanism is provided with a pair of pressing wheels, and the pressing wheels are abutted to the bottom roller; the fifth driving device is used for driving one end, located on the material feeding side of the stepping material pulling device, of the lifting rod mechanism to press downwards, and the pressure adjusting rod is adjustably arranged above one end, close to the pressing wheel, of the lifting rod mechanism and is abutted to the lifting rod mechanism through a spring. The material belt is pulled through the stepping pulling device, so that the material belt is more stable to move, and the operation rhythm of the whole machine is better matched.
According to some embodiments of the present invention, the top-cut detection carrier tape packaging machine further comprises an unwinding and winding device, the unwinding and winding device is disposed at a feeding side of the CCD detection device, and is used for unwinding the material tape; the unwinding and winding device comprises a diaphragm winding shaft, a material belt shaft, an unwinding mounting frame, a material belt positioning seat, a floating tension roller, a sixth driving device and a seventh driving device; the material belt shaft is arranged at one end of the unreeling mounting rack, the material belt positioning seat is arranged at the other end of the unreeling mounting rack, the diaphragm reeling shaft is arranged above the material belt shaft, and the floating tension roller is arranged adjacent to the material belt positioning seat; the sixth driving device is used for driving the diaphragm winding shaft to rotate, and the seventh driving device is used for driving the material belt shaft to rotate. Through unreeling and coiling mechanism, can realize unreeling and the recovery of the diaphragm that attaches in the material area of material area simultaneously.
According to some embodiments of the present invention, the material taking mechanism comprises a suction nozzle, a material taking mounting block, a guide block and a guide rod, the suction nozzle passes through the material taking mounting block and is movably connected with the material taking mounting block, the guide block is connected with the upper end of the suction nozzle, a spring is arranged between the guide block and the material taking mounting block, the guide rod is fixedly arranged on the material taking mounting block, and the guide rod is slidably connected with the guide block; the turntable fixing frame is also provided with a pressing mechanism, the number of the pressing mechanisms corresponds to that of the second driving devices, and the pressing mechanism comprises a pressing mounting plate and a pressing block; the push-down mounting plate is arranged on the side of the turntable fixing frame, the pressing block is connected with the push-down mounting plate in a sliding mode, one end of the pressing block is connected with the output end of the second driving device through a cam, and the other end of the pressing block is connected with the guide block.
According to some embodiments of the present invention, a carrier tape cover plate is further disposed on the upper side surface of the carrier tape guide rail, a carrier tape slot is formed between the carrier tape cover plate and the carrier tape guide rail, and material guides are further disposed at both ends of the carrier tape guide rail and aligned with the carrier tape slot; the heat sealing mechanism comprises an eighth driving device, a heat insulation block and a heat sealing knife assembly, one side of the heat insulation block is connected with the output end of the eighth driving device, and the heat sealing knife assembly is connected with the heat insulation block. Through the setting of strap groove, carry on spacingly to the carrier band, prevent that the carrier band from taking place crooked at the in-process that the packing removed.
According to some embodiments of the present invention, the feeding mechanism comprises a feeding mounting frame, a material shaft, a material stop plate, a material guide shaft and a rotary guide shaft, wherein one end of the material shaft is movably connected with the upper part of the feeding mounting frame, the material stop plate is arranged at two ends of the material shaft, and one end of the material guide shaft is connected with the middle part of the feeding mounting frame; the lower part of the feeding mounting frame is provided with a sector groove, and the rotary guide shaft is adjustably arranged in the sector groove. The feeding speed is changed by adjusting the rotary guide shaft.
According to some embodiments of the present invention, the CCD detecting device comprises a lens module, a lens mounting block, a support column, and an annular light source; the lens mounting block is sleeved on the supporting column and can adjust the position along the supporting column; the lens module is connected with the lens mounting block through a fine adjustment mounting seat, and the annular light source is arranged below the lens module. Through the arrangement, the height of the lens module is adjusted as required, and the lens module can be better focused by adjusting the fine adjustment mounting seat.
According to some embodiments of the utility model, CID detection device includes CID tool, first horizontal fine setting installation piece and first vertical fine setting mount table, first horizontal fine setting installation piece with the expansion end of first vertical fine setting mount table is connected, the CID tool with the expansion end of first horizontal fine setting installation piece is connected. Through this setting, can finely tune the position of CID tool as required, make its adaptation degree with the multistation carousel transfer device higher.
According to some embodiments of the present invention, the positioning and guiding device comprises a ninth driving device, a rotary jig, a movable mounting plate, a second transverse fine-tuning mounting block, and a second longitudinal fine-tuning mounting table; the second transverse fine-tuning installation block is connected with the movable end of the second longitudinal fine-tuning installation table, the movable installation plate is connected with the movable end of the second transverse fine-tuning installation block, the ninth driving device is arranged on the movable installation plate, and the rotary jig is connected with the output end of the ninth driving device. Through this setting, can finely tune the position of rotating jig as required, make between it and other devices the degree of cooperation higher.
According to some embodiments of the present invention, the top cutting device comprises a jig knife edge, a top cutting mounting frame, a tenth driving device and a top cutting punch; a material guide through groove is formed in the upper end face of the top cutting mounting frame, and the tool edge of the jig is arranged on the material guide through groove; the top cutting punch is arranged in the top cutting mounting frame and is in sliding connection with the top cutting mounting frame through a guide pillar and a guide sleeve, and the top cutting punch corresponds to the position of the tool edge of the jig; the output end of the tenth driving device is connected with the top cutting punch through an eccentric wheel mechanism. Through this setting, the guide leads to the groove and can carry on spacingly to the material area, prevents that the material area is crooked, pushes up and cuts the drift under the cooperation of guide pillar guide pin bushing, and the removal is stable, guarantees to push up the accuracy of cutting.
Additional aspects and advantages of the invention will be set forth in part in the description which follows and, in part, will be obvious from the description, or may be learned by practice of the invention.
Drawings
The above and/or additional aspects and advantages of the present invention will become apparent and readily appreciated from the following description of the embodiments, taken in conjunction with the accompanying drawings of which:
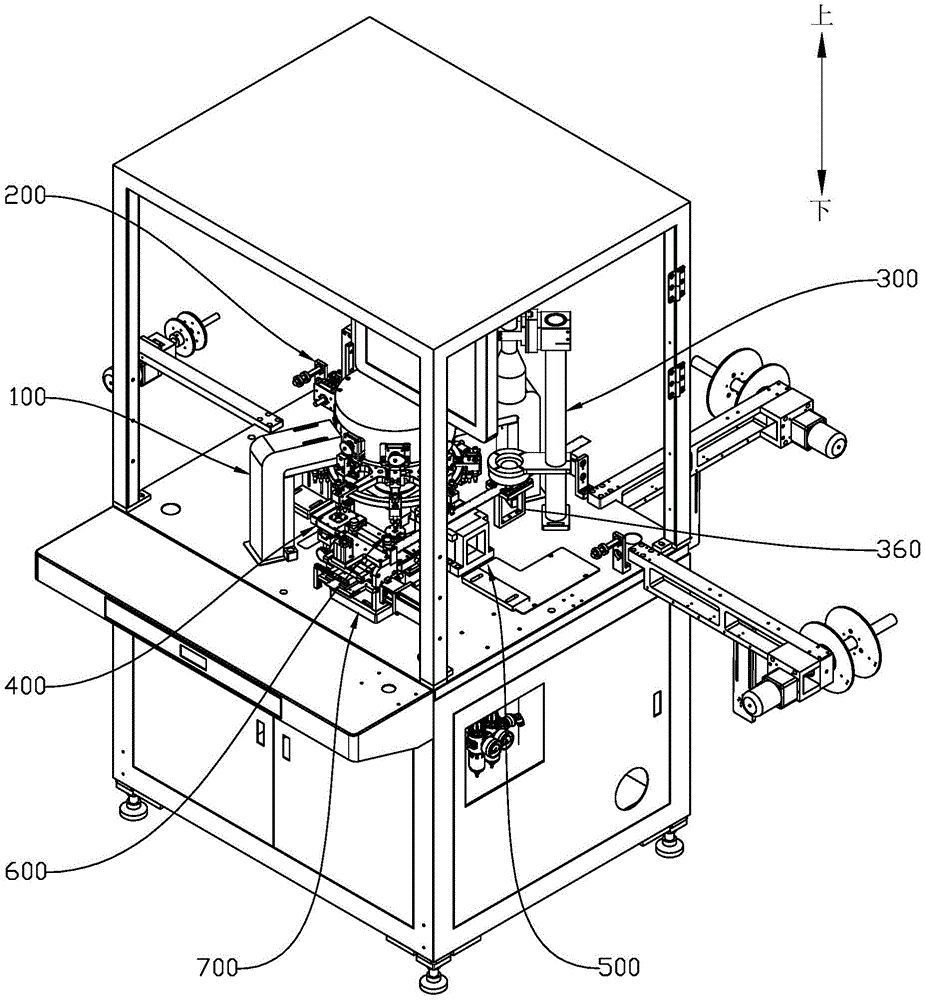
fig. 1 is a schematic view of a top-cutting detection carrier tape packaging machine according to an embodiment of the present invention;
fig. 2 is a schematic view of a carrier tape heat-seal packaging module of the carrier tape packaging machine for top-cut detection according to an embodiment of the present invention;
fig. 3 is a schematic view of a CCD detecting device of a carrier tape packaging machine for top cut detection according to an embodiment of the present invention;
fig. 4 is a schematic view of a CID detection device of a top-cut detection carrier tape packaging machine according to an embodiment of the present invention;
fig. 5 is a schematic view of a top cutting device of a top cutting detection carrier tape packaging machine according to an embodiment of the present invention;
fig. 6 is a schematic view of a positioning and guiding device of a top-cut detection carrier tape packaging machine according to an embodiment of the present invention;
fig. 7 is a schematic view of a discharge side of a step-by-step pulling device of a carrier tape packaging machine according to an embodiment of the present invention;
fig. 8 is a schematic view of an unwinding and winding device of a top-cut detection carrier tape packaging machine according to an embodiment of the present invention;
fig. 9 is a schematic view of a multi-station turntable transferring device of a top-cutting detection carrier tape packaging machine according to an embodiment of the present invention;
fig. 10 is a schematic view of the feeding side of the step-by-step pulling device of the carrier tape packaging machine according to the embodiment of the present invention.
Reference numerals: the multi-station turntable transferring device 100, the first driving device 110, the second driving device 120, the multi-station turntable 130, the material taking mechanism 140, the suction nozzle 141, the material taking installation block 142, the guide block 143, the guide rod 144, the turntable fixing frame 150, the downward pressing mechanism 151, the downward pressing installation plate 1511, the pressing block 1512, the disc 152, the turntable supporting seat 153, the carrier tape heat-seal packaging module 200, the carrier tape guide rail 210, the ratchet shaft 211, the material guide 212, the third driving device 213, the carrier tape cover plate 214, the carrier tape groove 215, the guide rail installation seat 216, the movable clamping plate 2161, the feeding mechanism 220, the feeding installation rack 221, the sector-shaped groove 2211, the material shaft 222, the material baffle 223, the material guide shaft 224, the rotating guide shaft 225, the heat-seal mechanism 230, the eighth driving device 231, the heat insulation block 232, the heat-seal cutter component 233, the CCD detection device 300, the lens module 310, the lens installation block 320, the support column 330, the annular light source 340, the fine-adjusting installation seat 350, the fine-adjustment installation seat, A material belt limiting seat 360, a CID detection device 400, a CID jig 410, a first transverse fine-adjustment mounting block 420, a first longitudinal fine-adjustment mounting table 430, a top-cutting device 500, a jig knife edge 510, a top-cutting mounting frame 520, a material guide through groove 521, a tenth driving device 530, a top-cutting punch 540, an eccentric wheel mechanism 541, a positioning and guiding device 600, a ninth driving device 610, a rotary jig 620, a movable mounting plate 630, a second transverse fine-adjustment mounting block 640, a second longitudinal fine-adjustment mounting table 650, a stepping material pulling device 700, a material pulling frame 710, a fourth driving device 720, a fifth driving device 730, a bottom roller 740, a pressure adjusting rod 750, a lifting rod mechanism 760, a pinch roller 761, a lifting material belt lateral plate 762, a first long rod 763, a second long rod 764, a third long rod 765, an unreeling and reeling device 800, a membrane reeling shaft 810, a unreeling mounting frame 830, a material belt positioning seat 840, a limiting block 841, a floating roller 850, a material belt 763, a second long rod 764, a material belt winding mechanism, a material belt wrapping machine with a material belt bundling mechanism, a material belt winding mechanism with a large diameter, a small number of which is small size and a small size, A sixth driving device 860, a seventh driving device 870, a winding support frame 880 and a transition guide wheel 890.
Detailed Description
Reference will now be made in detail to the embodiments of the present invention, examples of which are illustrated in the accompanying drawings, wherein like reference numerals refer to the same or similar elements or elements having the same or similar functions throughout. The embodiments described below with reference to the drawings are exemplary only for the purpose of explaining the present invention, and should not be construed as limiting the present invention.
In the description of the present invention, it should be understood that the orientation or positional relationship indicated with respect to the orientation description, such as up, down, front, rear, left, right, etc., is based on the orientation or positional relationship shown in the drawings, and is only for convenience of description and simplification of description, and does not indicate or imply that the device or element referred to must have a specific orientation, be constructed and operated in a specific orientation, and thus, should not be construed as limiting the present invention.
In the description of the present invention, a plurality of means are one or more, a plurality of means are two or more, and the terms greater than, less than, exceeding, etc. are understood as not including the number, and the terms greater than, less than, within, etc. are understood as including the number. If the first and second are described for the purpose of distinguishing technical features, they are not to be understood as indicating or implying relative importance or implicitly indicating the number of technical features indicated or implicitly indicating the precedence of the technical features indicated.
In the description of the present invention, unless there is an explicit limitation, the words such as setting, installation, connection, etc. should be understood in a broad sense, and those skilled in the art can reasonably determine the specific meanings of the above words in combination with the specific contents of the technical solution.
The following describes a top-cut inspection carrier tape packaging machine according to an embodiment of the present invention with reference to the drawings.
According to the utility model discloses top is cut and is detected carrier band packagine machine, move including the multistation carousel and carry device 100, carrier band heat-seal packing module 200, CCD detection device 300, CID detection device 400, top and cut device 500 and location guider 600.
As shown in fig. 1, fig. 2 and fig. 9, the multi-station turntable transferring device 100 includes a first driving device 110, a multi-station turntable 130, a plurality of material taking mechanisms 140, a turntable fixing frame 150 and a second driving device 120, wherein the multi-station turntable 130 is movably disposed below the turntable fixing frame 150, the material taking mechanisms 140 are disposed at stations of the multi-station turntable 130, the first driving device 110 is used for driving the multi-station turntable 130 to rotate, and the second driving device 120 is used for driving the material taking mechanisms 140 to take materials; the carrier band heat-seal packaging module 200 is arranged on one side of the multi-station turntable transfer device 100, the carrier band heat-seal packaging module 200 comprises a carrier band guide rail 210, a feeding mechanism 220 and a heat-seal mechanism 230, the carrier band guide rail 210 comprises a ratchet wheel and a third driving device 213, the ratchet wheel is arranged at one end in the carrier band guide rail 210, the third driving device 213 is used for driving the ratchet wheel to drive a carrier band to move, the feeding mechanism 220 is arranged above the carrier band guide rail 210, and the heat-seal mechanism 230 is arranged between the feeding mechanism 220 and the carrier band guide rail 210; the CCD detection device 300 is arranged at the outer side of the multi-station turntable transfer device 100 and is used for detecting products; the CID detection device 400 is arranged at the outer side of the multi-station turntable transfer device 100 and is used for detecting the flatness of the product; the top cutting device 500 is arranged at the outer side of the multi-station turntable transferring device 100 and is positioned between the CCD detection device 300 and the CID detection device 400, and the top cutting device 500 is used for cutting off products from the material belt; and a positioning guide 600 disposed between the CID detection device 400 and the top cutting device 500, the positioning guide 600 being used to change the direction of the product.
As shown in fig. 1, the top-cut detecting carrier tape packaging machine further includes a case, and a mounting table is disposed in the case. The multi-station turntable shifting device 100 is arranged in the middle of the installation platform, the CCD detection device 300 and the top cutting device 500 are arranged on the same side of the multi-station turntable shifting device 100 and are positioned on the same straight line, and the top cutting device 500 is positioned right below one of the stations of the multi-station turntable shifting device 100; the positioning guide device 600 is arranged right below the station of the multi-station turntable transfer device 100 adjacent to the top cutting device 500; the CID detection device 400 is provided directly below the station adjacent to the positioning guide device 600 of the multi-station carousel transfer device 100.
As shown in fig. 9, in the multi-station turntable transferring device 100, the first driving device 110 is a stepping motor and is disposed below the multi-station turntable 130, an output end of the first driving device 110 is connected to a central axis of the multi-station turntable 130, the turntable fixing frame 150 includes two turntable supporting seats 153 and a turntable 152 corresponding to the multi-station turntable 130, and the turntable 152 is fixedly disposed above and aligned with the multi-station turntable 130 through the turntable supporting seats 153; eight material taking mechanisms 140, namely eight stations, are uniformly arranged on the outer side of the multi-station turntable 130, eight second driving devices 120 are uniformly arranged on the disc 152, and the material taking mechanisms 140 correspond to the second driving devices 120 one by one.
According to the utility model discloses top is cut and is detected carrier band packagine machine, the material area passes through CCD detection device 300 and top in proper order and cuts device 500, CCD detection device 300 detects the back to the product in material area, top is cut device 500 and is cut the product that has detected from the material area off, multistation carousel moves and carries device 100 and shifts the product from top is cut device 500 and shift location guider 600, location guider 600 leads the product grade after, multistation carousel moves and carries device 100 and shifts the product after leading to CID detection device 400 and carry out the plane degree and detect, last multistation carousel moves and carries the device and shifts the qualified product that detects to the carrier band of heat-seal packaging module 200 on, carrier band heat-seal packaging module 200 heat-seal the product and pack on carrying the area; under the effect that the multistation carousel moved and carries device 100, steps such as above-mentioned CCD detects, top is cut, the position is led just, CID detects, carrier band packing can go on simultaneously, need not artifical supplementary, and production efficiency is high to the product can carry out comprehensive CCD and detect with CID, guarantees product quality, and the setting of carousel formula simultaneously can reduce the complete machine volume, saves space.
In some embodiments of the present invention, the top-cut detecting carrier tape packaging machine further includes a stepping pulling device 700, the stepping pulling device 700 and the CCD detecting device are respectively disposed at two sides of the top-cut device 500, and the feeding side and the discharging side of each device are all on the same straight line; the stepping material pulling device 700 comprises a material pulling frame 710, a fourth driving device 720, a fifth driving device 730, a rod lifting mechanism 760, a bottom roller 740 and a pressure adjusting rod 750; the bottom rollers 740 are rotatably arranged between the material pulling frames 710, and the fourth driving device 720 is used for driving the bottom rollers 740 to rotate; the middle part of the lifting rod mechanism 760 is movably connected with the inner walls of the two sides of the material pulling frame 710, the lifting rod mechanism 760 is positioned above the bottom roller 740, the lifting rod mechanism 760 is provided with a pair of press wheels 761, and the press wheels 761 are abutted with the bottom roller 740; the fifth driving device 730 is used for driving one end of the lifting rod mechanism 760 positioned on the feeding side of the stepping pulling device 700 to press down, and the pressure adjusting rod 750 is adjustably arranged above one end of the lifting rod mechanism 760 close to the pressing wheel 761 and is abutted against the lifting rod mechanism 760 through a spring.
As shown in fig. 7 and 10, two ends of the bottom roller 740 are respectively rotatably connected with the inner walls of two sides of the material pulling frame 710 and are located in the middle of the material pulling frame 710; the fourth driving device 720 is a motor, the fourth driving device 720 is disposed outside the material pulling frame 710, and an output end of the fourth driving device 720 is connected with one end of the bottom roller 740 to drive the bottom roller 740 to rotate. The material lifting mechanism consists of two material lifting side plates 762, a first long rod 763, a second long rod 764, a third long rod 765 and a pressing wheel 761, wherein one ends of the two material lifting side plates 762 close to the feeding side of the stepping material pulling device 700 are fixedly connected with two ends of the first long rod 763 respectively; the middle parts of the two material lifting side plates 762 are sleeved on the second long rod 764 through bearings, and two ends of the second long rod 764 are fixedly connected with the upper parts of the inner walls of the two sides of the material pulling frame 710; two ends of the third long rod 765 are respectively fixedly connected with the two lifting side plates 762 and located above the bottom roller 740, and the pair of pressing wheels 761 are sleeved on the third long rod 765 through bearings and abut against the bottom roller 740. The fifth driving device 730 is a cylinder and is disposed above the first long rod 763, the telescopic rod of the fifth driving device 730 is connected to a screw, and when the fifth driving device 730 works, the telescopic rod extends out to press the first long rod 763 downwards, so that the pressing wheel 761 is lifted. The two pressure adjusting rods 750 are respectively arranged above one end, provided with the pressing wheel 761, of the two material lifting side plates 762 and are in threaded connection with the upper end of the material pulling frame 710, the pressure adjusting rods 750 are abutted against the material lifting side plates 762 through springs, and the pressing wheel 761 is pressed against the bottom roller 740 under the action of the springs; the pressure between the pinch rollers 761 and the bottom roller 740 is adjusted by twisting the pressure adjustment rod, increasing or decreasing the pressure of the springs on the lifting side plate 762.
The pressing wheel 761 can be lifted up under the action of the fifth driving device, so that the material belt can be conveniently placed into the stepping pulling device 700; the pressure between the pressing roller 761 and the bottom roller 740 is adjusted as necessary by adjusting the pressure adjustment lever 750. Draw the material area through step-by-step material device 700 that draws for the removal in material area is more stable, coordinates the operation rhythm of complete machine better.
In some embodiments of the present invention, the top-cut detecting carrier tape packaging machine further includes an unwinding and winding device 800, the unwinding and winding device 800 is disposed at the feeding side of the CCD detecting device 300, and is used for unwinding the material tape; the unwinding and winding device 800 comprises a diaphragm winding shaft 810, a material belt shaft 820, an unwinding mounting frame 830, a material belt positioning seat 840, a floating tension roller 850, a sixth driving device 860 and a seventh driving device 870; the material belt shaft 820 is arranged at one end of the unreeling mounting frame 830, the material belt positioning seat 840 is arranged at the other end of the unreeling mounting frame 830, the diaphragm reeling shaft 810 is arranged above the material belt shaft 820, and the floating tension roller 850 is arranged adjacent to the material belt positioning seat 840; a sixth drive 860 is used to rotate the diaphragm take-up spool 810 and a seventh drive 870 is used to rotate the web spool 820.
As shown in fig. 8, the tape shaft 820 is used for placing a roll of tape, and two fixing plates are further disposed on the tape shaft 820 to fix the tape; the seventh driving device 870 is a motor and is disposed on two sides of one end of the unwinding mounting rack 830 and the material belt shaft 820, respectively, and an output end of the seventh driving device 870 is connected to the material belt shaft 820. The membrane winding shaft 810 is connected with the unwinding mounting frame 830 through a winding support frame 880, is located above the belt shaft 820, the sixth driving device 860 is a motor, is respectively arranged at two sides of the upper end of the rewinding support shaft with the membrane winding shaft 222, and the sixth driving device 860 is connected with the membrane winding shaft 222. The material belt positioning seat 840 is installed at the other end of the unreeling mounting frame 830, a pair of material belt limiting blocks 841 is further arranged on the upper end face of the material belt positioning seat 840, and the material belt limiting blocks 841 are formed between the material belt limiting blocks 841 and the upper end face of the material belt positioning seat 840; the floating tension roller 850 is arranged obliquely below the material belt positioning seat 840, and a pair of transition guide wheels 890 is arranged between the floating tension roller 850 and the material belt positioning seat 840. The material belt is led out from the material belt shaft 820 and bypasses below the floating tension roller 850, and then passes through the two transition guide wheels 890, the diaphragm on the material belt is torn down and drawn to the diaphragm rolling shaft 810, and the material belt with the diaphragm torn off enters the material belt limiting block 841; when the material belt moves, the floating pressure roller receives the upward traction force of the material belt, senses the movement of the material belt, controls the sixth driving device 860 to work, and the diaphragm rolling shaft 810 peels and rolls the diaphragm from the material belt. Due to the arrangement of the material belt positioning seat 840, when the material belt is unreeled and enters the CCD detection device 300, the position is accurate, and the material belt is not prone to being skewed; through unreeling and coiling mechanism 800, can realize unreeling of material area and the recovery of the diaphragm that the material area is attached simultaneously.
As shown in fig. 9, in some embodiments of the present invention, the material taking mechanism 140 includes a suction nozzle 141, a material taking mounting block 142, a guide block 143, and a guide rod 144, the suction nozzle 141 passes through the material taking mounting block 142 and is movably connected to the material taking mounting block 142, the guide block 143 is connected to the upper end of the suction nozzle 141, a spring is disposed between the guide block 143 and the material taking mounting block 142, the guide rod 144 is fixedly disposed on the material taking mounting block 142, and the guide rod 144 is slidably connected to the guide block 143; the turntable fixing frame 150 is further provided with a pressing mechanism 151, the number of the pressing mechanisms 151 corresponds to that of the second driving devices 120, and the pressing mechanism 151 comprises a pressing mounting plate 1511 and a pressing block 1512; the downward-pressing mounting plate 1511 is arranged at the side of the turntable fixing frame 150, the press block 1512 is slidably connected with the downward-pressing mounting plate 1511, one end of the press block 1512 is connected with the output end of the second driving device 120 through a cam, and the other end of the press block 1512 is connected with the guide block 143.
Eight downward pressing mechanisms 151 are uniformly arranged on the outer side of the disc 152 of the turntable fixing frame 150, and the downward pressing mechanisms 151 correspond to the material taking mechanisms 140 one by one; the lower pressing mounting plate 1511 is connected with the outer side surface of the disc 152, the pressing block 1512 and the lower pressing mounting plate 1511 are connected with the sliding block in a sliding manner through the sliding rail, and the lower end of the pressing block 1512 is abutted against the guide block 143; the second driving device 120 is a stepping motor, the second driving device 120 corresponds to the pressing mechanisms 151 one by one, the second driving device 120 is disposed on the upper end surface of the disc 152 and is connected to the side surface of the pressing mounting plate 1511, and the output end of the second driving device 120 passes through the pressing mounting plate 1511 and is connected to the pressing block 1512 through a cam structure. The multi-station turntable transferring device 100 works: the second driving device 120 drives the pressing block 1512 to perform regular up-and-down movement, the multi-station turntable 130 performs rotation matched with the first device under the driving of the first device, and when the multi-station turntable 130 rotates, the second driving device 120 drives the pressing block 1512 to move upwards; when the multi-station turntable 130 finishes rotating and the guide block 143 of the material taking device is aligned with the press block 1512, the second driving device 120 drives the press block 1512 to press down, so that the guide block 143 is pressed down, and the suction nozzle 141 moves down to suck a product or place the product; after the material taking or product placing is completed, the multi-station turntable 130 rotates, the pressing block 1512 is separated from the guide block 143 and staggered, and the suction nozzle 141 is reset under the action of the spring.
In some embodiments of the present invention, a carrier cover plate 214 is further disposed on the upper side of the carrier guide rail 210, a carrier tape slot 215 is formed between the carrier cover plate 214 and the carrier guide rail 210, material guides 212 are further disposed at two ends of the carrier guide rail 210, and the material guides 212 are aligned with the carrier tape slot 215; the heat-seal mechanism 230 includes an eighth driving device 231, a heat insulating block 232, and a heat-seal blade assembly 233, wherein one side of the heat insulating block 232 is connected to an output end of the eighth driving device 231, and the heat-seal blade assembly 233 is connected to the heat insulating block 232.
As shown in fig. 2, the carrier tape guide 210 includes two identical long blocks and two guide rail mounting seats 216, a pair of adjustable movable clamping plates 2161 is disposed on the guide rail mounting seats 216, the two long blocks are disposed between the movable clamping plates 2161 and respectively fixedly connected with the movable clamping plates 2161, and the guide rail mounting seats 216 are disposed at two ends of the long blocks; the carrier cover plate 214 is disposed on the upper side of the long blocks, a carrier groove 215 is formed between the long blocks, and the carrier grooves 215 of the two long blocks are opposite. By adjusting the distance between the movable clamping plates 2161, the distance between the long blocks can be adjusted, and the width of the carrier tape guide rail 210 can be changed, so that carrier tapes with different widths can be adapted. Through the setting of strap groove 215, carry on spacingly to the carrier band, prevent that the carrier band from taking place crooked in the in-process that the packing removed.
The ratchet wheel is arranged at one end of the carrier tape guide rail 210 and is rotatably arranged between the two long strip blocks through a ratchet wheel shaft 211; the third driving device 213 is a stepping motor, and is arranged outside the long bar block, and the output end of the third driving device 213 is connected with one end of the ratchet shaft 211; the heat seal mechanism 230 is disposed above the side of the ratchet wheel facing the inside of the carrier tape guide 210, the eighth driving device 231 is a slide table cylinder, the heat insulating block 232 is disposed on the slide table of the eighth driving device 231, and the heat seal blade assembly 233 is disposed at the lower end of the heat insulating block 232. The ratchet wheel is hooked with a groove or a hole on the lower side surface of the carrier tape in the carrier tape guide 210, and the third driving device 213 drives the ratchet wheel to rotate towards the outer direction of the carrier tape guide 210, so as to draw the carrier tape to move in the carrier tape guide 210; meanwhile, the eighth driving device 231 drives the heat-sealing knife assembly 233 to press down to heat-seal and package the carrier tape.
As shown in fig. 2, the guiding members 212 are guiding rails with gentle curvature, wherein one end of one guiding member 212 is connected to the feeding end of the carrier tape guiding rail 210 and aligned with the carrier tape slot 215; one end of another guide 212 is attached to the discharge end of the carrier tape guide 210 and is also aligned with the carrier tape slot 215. Through the arrangement of the material guiding piece 212, the carrier tape is prevented from being scratched due to the gradual transition of the material guiding piece 212 when the carrier tape enters and exits the carrier tape guide rail 210.
As shown in fig. 2, in some embodiments of the present invention, the feeding mechanism 220 includes a feeding mounting frame 221, a material shaft 222, a material baffle 223, a material guiding shaft 224 and a rotary guiding shaft 225, one end of the material shaft 222 is movably connected to the upper portion of the feeding mounting frame 221, the material baffle 223 is disposed at two ends of the material shaft 222, and one end of the material guiding shaft 224 is connected to the middle portion of the feeding mounting frame 221; the lower portion of the feeder mount 221 is provided with a sector-shaped slot 2211, and the rotary guide shaft 225 is adjustably disposed in the sector-shaped slot 2211. The feed rate is varied by adjusting the rotating guide shaft 225.
During operation, the packaging coil material of the carrier tape is arranged on the material shaft 222 and is positioned between the material baffle plates 223; the web of packaging material is pulled from the supply reel 222, around the supply reel 224 and the rotary guide 225, between the heat sealing mechanism 230 and the carrier tape, and is then wrapped by the heat sealing mechanism 230.
In some embodiments of the present invention, the CCD detecting device 300 includes a lens module 310, a lens mounting block 320, a supporting column 330, and an annular light source 340; the lens mounting block 320 is sleeved on the supporting column 330 and can be adjusted in position along the supporting column 330; the lens module 310 is connected to the lens mounting block 320 through the fine adjustment mounting seat 350, and the annular light source 340 is disposed below the lens module 310. Through this arrangement, the height of the lens module 310 can be adjusted as required, and the position of the lens can be adjusted by rotating the knob of the fine adjustment mounting base 350, so that the lens module 310 can focus better.
As shown in fig. 3, the CCD detecting device 300 further includes a material belt limiting seat 360, the material belt limiting seat 360 is disposed below the annular light source 340, and the material belt corresponds to the hollow portion of the annular light source 340 when in the material belt limiting seat 360, and the lens of the lens module 310 is aligned with the hollow portion of the annular light source 340, and can be aligned with the product on the material belt through the annular light source 340; the material inlet and the material outlet of the material belt limiting seat 360 are both in the same straight line and have the same height as the material inlet of the top cutting device 500. The lens mounting block 320 is connected with the supporting column 330 in a loose and tight manner through the tightness of the screw, so that the position of the lens mounting block 320 on the supporting column 330 can be adjusted; in the present invention, the lens mounting block 320 may be, but is not limited to, connected to the supporting column 330 in the above manner.
As shown in fig. 4, in some embodiments of the present invention, the CID detection device 400 includes a CID fixture 410, a first horizontal fine-tuning installation block 420 and a first vertical fine-tuning installation block 430, the first horizontal fine-tuning installation block 420 is connected to the movable end of the first vertical fine-tuning installation block 430, and the CID fixture 410 is connected to the movable end of the first horizontal fine-tuning installation block 420. The CID jig 410 needs to be aligned with one of the material taking mechanisms 140 of the multi-station turntable transferring device 100, and the position of the CID jig 410 can be adjusted by rotating the knobs of the first transverse fine-tuning installation block 420 and the first longitudinal fine-tuning installation table 430. Through this setting, can finely tune the position of CID tool 410 as required, make its adaptation degree with multistation carousel transfer device 100 higher.
As shown in fig. 6, in some embodiments of the present invention, the positioning guide 600 includes a ninth driving device 610, a rotating fixture 620, a moving mounting plate 630, a second lateral fine-tuning mounting block 640, and a second longitudinal fine-tuning mounting table 650; the second transverse fine-tuning mounting block 640 is connected with the movable end of the second longitudinal fine-tuning mounting table 650, the movable mounting plate 630 is connected with the movable end of the second transverse fine-tuning mounting block 640, the ninth driving device 610 is arranged on the movable mounting plate 630, and the rotary jig 620 is connected with the output end of the ninth driving device 610. The ninth driving device 610 is a stepping motor, the ninth driving device 610 is connected to the lower end surface of the movable mounting plate 630, and the output end of the ninth driving device 610 penetrates through the movable mounting plate 630 and is connected to the lower end of the rotary jig 620 arranged above the movable mounting plate 630; the position of the moving mounting plate 630 can be adjusted by turning the knobs of the second lateral fine adjustment mounting block 640 and the second longitudinal fine adjustment mounting table 650. Through this setting, can finely tune the position of rotating jig 620 as required, make between it and other devices the degree of cooperation higher.
In some embodiments of the present invention, the top cutting apparatus 500 comprises a jig blade 510, a top cutting mounting frame 520, a tenth driving device 530, and a top cutting punch 540; a material guide through groove 521 is formed in the upper end face of the top cutting mounting frame 520, and the jig knife edge 510 is arranged on the material guide through groove 521; the top cutting punch 540 is arranged in the top cutting mounting frame 520 and is in sliding connection with the top cutting mounting frame 520 through a guide pillar and a guide sleeve, and the top cutting punch 540 corresponds to the tool edge 510; the output of the tenth drive 530 is connected to the top cutting punch 540 via an eccentric mechanism 541. Through this setting, the logical groove 521 of guide can carry on spacingly to the material area, prevents that the material area is crooked, and top is cut drift 540 under the cooperation of guide pillar guide pin bushing, and the removal is stable, guarantees the accuracy of top cutting.
As shown in fig. 5, the top-cutting mounting frame 520 is composed of an upper mounting plate, two vertical support plates, and a bottom mounting plate, wherein one ends of the two vertical support plates are respectively disposed at two sides of the lower end surface of the upper mounting plate, and the other ends are connected to the bottom mounting plate. The material guide through groove 521 is arranged in the middle of the upper mounting plate, and the jig knife edge 510 is arranged above the material guide through groove 521; the tool edge 510 is a square plate with a middle part provided with a cutting edge through hole, the cutting edge through hole is aligned with the material guiding through groove 521, and the cutting edge faces the material guiding through groove 521. The top cutting punch 540 is arranged between the two vertical supporting plates, the guide pillar is arranged between the upper mounting plate and the bottom mounting plate, and the top cutting punch 540 is connected with the guide pillar in a sliding manner through the guide sleeve; the tenth driving device 530 is a servo motor, is disposed below the bottom mounting plate, and is connected to the bottom of the top cutting punch 540 through an eccentric mechanism 541, that is, the output end of the tenth driving device 530 is connected to an eccentric wheel, and the eccentric wheel is connected to the lower end of the top cutting punch 540 through a connecting rod.
In the description herein, references to the description of the term "one embodiment," "some embodiments," "an illustrative embodiment," "an example," "a specific example," or "some examples" or the like mean that a particular feature, structure, material, or characteristic described in connection with the embodiment or example is included in at least one embodiment or example of the present invention. In this specification, the schematic representations of the terms used above do not necessarily refer to the same embodiment or example. Furthermore, the particular features, structures, materials, or characteristics described may be combined in any suitable manner in any one or more embodiments or examples.
While embodiments of the present invention have been shown and described, it will be understood by those of ordinary skill in the art that: various changes, modifications, substitutions and alterations can be made to the embodiments without departing from the principles and spirit of the invention, the scope of which is defined by the claims and their equivalents.