SUMMERY OF THE UTILITY MODEL
To the technical problem that prior art exists, the utility model provides a welding jig for loading arm equipment.
In order to achieve the above object, the utility model provides a following technical scheme: a welding fixture for assembling a loading machine movable arm comprises a base, wherein a seat beam positioning mechanism is arranged on the base, a movable arm plate positioning mechanism I and a movable arm plate positioning mechanism II are respectively arranged on two sides of the seat beam positioning mechanism, the seat beam positioning mechanism comprises a seat beam positioning support and a seat beam supporting seat, a positioning mandrel and a positioning bolt I are arranged on the seat beam positioning support, and the positioning bolt I is arranged below the positioning mandrel; the first movable arm plate positioning mechanism comprises a first base plate, a T-shaped block and a positioning block, the first base plate is connected to the base, the T-shaped block is connected to the first base plate, the positioning block is arranged on the T-shaped block, and U-shaped positioning grooves are formed in the T-shaped block and the positioning block; the second movable arm plate positioning mechanism comprises a second bottom plate connected to the base and two support plates oppositely arranged on the second bottom plate, baffles are arranged on the support plates, a second positioning bolt is arranged between the two baffles and connected to the connecting plate, and the connecting plate is arranged on the support plates.
Preferably, two V-shaped positioning grooves for placing the positioning mandrels are oppositely arranged on the seat beam positioning bracket.
Preferably, T type piece includes the riser of vertical setting and the flat board of level setting, riser and dull and stereotyped junction are located to the locating piece, and the vertical extension of U type constant head tank on the locating piece, and U type constant head tank on the T type piece is located on the flat board and the horizontal extension.
Preferably, a cushion block is obliquely arranged between the two support plates.
Preferably, a movable arm plate auxiliary positioning mechanism is arranged between the seat beam positioning mechanism and the movable arm plate positioning mechanism I and between the seat beam positioning mechanism and the movable arm plate positioning mechanism II, the movable arm plate auxiliary positioning mechanism comprises a base plate III connected to the base and two side plates oppositely arranged on the base plate III, one side plate is provided with a positioning auxiliary block, and the other side plate is connected with a positioning bolt III.
Preferably, a movable arm plate supporting seat is arranged between the first movable arm plate positioning mechanism and the second movable arm plate positioning mechanism.
The utility model discloses still including enabling the other subassemblies that a welding jig normally used for loader arm equipment, be the conventional technological means in this field. In addition, the device or the component which is not limited in the utility model adopts the conventional technical means in the field.
The utility model discloses can carry out accuracy, fix a position reliably to the swing arm of unidimensional not, realize the fast switch-over of like product and assemble, the suitability is strong, guarantees welded quality.
Drawings
Fig. 1 is a schematic view of a structure for loading a boom in the related art.
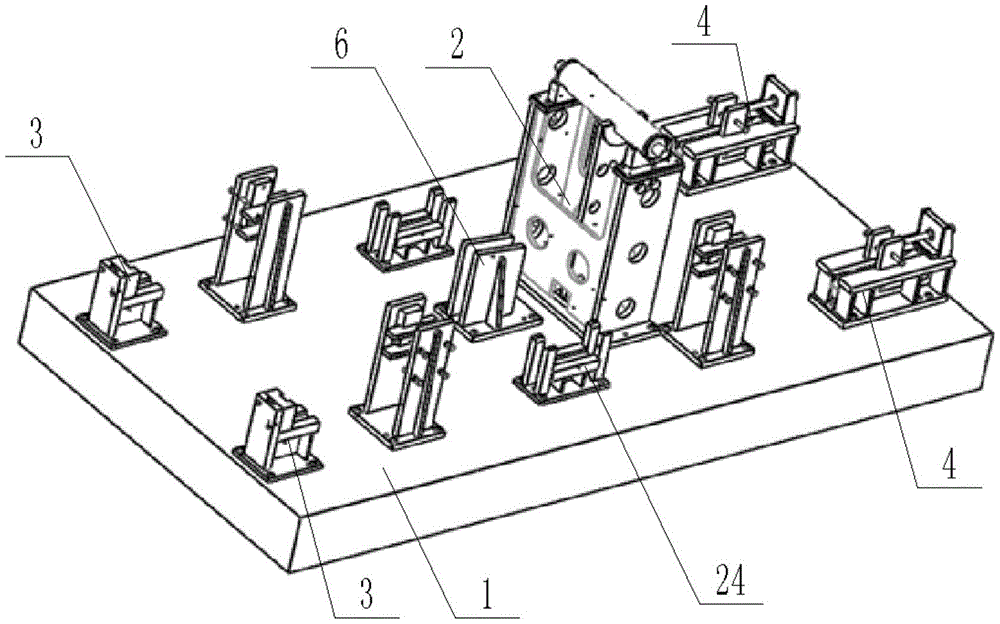
Fig. 2 is a schematic structural diagram of the present embodiment.
Fig. 3 is a schematic structural view of the seat beam positioning bracket of fig. 2.
Fig. 4 is a schematic structural diagram of the first boom plate positioning mechanism in fig. 2.
Fig. 5 is a schematic structural diagram of the second boom plate positioning mechanism in fig. 2.
Fig. 6 is a schematic structural view of the boom plate assist positioning mechanism of fig. 2.
Fig. 7 is a schematic structural view of the use state of the present embodiment.
In the figure: the movable arm plate positioning device comprises a base 1, a seat beam positioning mechanism 2, a movable arm plate positioning mechanism I3, a movable arm plate positioning mechanism II 4, a seat beam positioning support 5, a seat beam supporting seat 6, a positioning mandrel 7, a positioning bolt I8, a base plate I9, a base plate I10T-shaped block 10, a positioning block 11, a positioning block 12U-shaped positioning groove 13, a base plate II 14, a supporting plate 15, a positioning bolt II 16, a positioning bolt II 17V-shaped positioning groove 18, a cushion block 19, a movable arm plate auxiliary positioning mechanism 20, a base plate III 21, a side plate 22, a positioning auxiliary block 23, a movable arm plate supporting seat 24.
Detailed Description
The technical solution of the present invention will be described clearly and completely with reference to the accompanying drawings, and obviously, the described embodiments are some, but not all embodiments of the present invention. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
In the description of the present invention, it should be noted that the terms "center", "upper", "lower", "left", "right", "vertical", "horizontal", "inner", "outer", and the like indicate orientations or positional relationships based on the orientations or positional relationships shown in the drawings, and are only for convenience of description and simplification of description, but do not indicate or imply that the device or element referred to must have a specific orientation, be constructed and operated in a specific orientation, and thus, should not be construed as limiting the present invention. Furthermore, the terms "first," "second," and "third" are used for descriptive purposes only and are not to be construed as indicating or implying relative importance.
In the description of the present invention, it is to be noted that, unless otherwise explicitly specified or limited, the terms "mounted," "connected," and "connected" are to be construed broadly, and may be, for example, fixedly connected, detachably connected, or integrally connected; can be mechanically or electrically connected; they may be connected directly or indirectly through intervening media, or they may be interconnected between two elements. The specific meaning of the above terms in the present invention can be understood in specific cases to those skilled in the art.
Examples
Referring to fig. 2-7, a welding fixture for assembling a loader arm comprises a base 1, wherein a seat beam positioning mechanism 2 is arranged on the base 1, a movable arm plate positioning mechanism 3 and a movable arm plate positioning mechanism II 4 are respectively arranged on two sides of the seat beam positioning mechanism 2, the seat beam positioning mechanism 2 comprises a seat beam positioning support 5 and a seat beam supporting seat 6, a positioning mandrel 7 and a positioning bolt I8 are arranged on the seat beam positioning support 5, and the positioning bolt I8 is arranged below the positioning mandrel 7; the first movable arm plate positioning mechanism comprises a first bottom plate 9, a T-shaped block 10 and a positioning block 11, the first bottom plate 9 is connected to the base 1, the T-shaped block 10 is connected to the first bottom plate, the positioning block 11 is arranged on the T-shaped block 10, and U-shaped positioning grooves 12 are formed in the T-shaped block 10 and the positioning block 11; the second movable arm plate positioning mechanism 4 comprises a second bottom plate 13 connected to the base 1 and two support plates 14 oppositely arranged on the second bottom plate 13, baffles 15 are arranged on the support plates 14, a second positioning bolt 16 is arranged between the two baffles 15, the second positioning bolt 16 is connected to a connecting plate, and the connecting plate is arranged on the support plates 14.
Two V-shaped positioning grooves 17 for placing the positioning core shaft 7 are oppositely arranged on the seat beam positioning support 5. The V-shaped positioning groove can reliably position the positioning mandrels with different diameters, so that the V-shaped positioning groove is suitable for seat beams with through holes with different inner diameters.
T type piece 10 includes the riser of vertical setting and the flat board of level setting, riser and dull and stereotyped junction are located to locating piece 11, and the vertical extension of U type constant head tank 12 on the locating piece 11, and U type constant head tank 12 on the T type piece 10 is located on the flat board and the level extends.
A cushion block 18 is obliquely arranged between the two support plates 14. The inclination angle of cushion and the inclined plane phase-match of moving the arm board tip, the cushion can support moving the arm board's tip.
And movable arm plate auxiliary positioning mechanisms 19 are arranged between the seat beam positioning mechanism 2 and the movable arm plate positioning mechanism I3 and between the seat beam positioning mechanism 2 and the movable arm plate positioning mechanism II 4, each movable arm plate auxiliary positioning mechanism 19 comprises a base plate III 20 connected to the base 1 and two side plates 21 arranged on the base plate III 20 oppositely, one side plate 21 is provided with a positioning auxiliary block 22, and the other side plate 21 is connected with a positioning bolt III 23.
And a movable arm plate supporting seat 24 is arranged between the movable arm plate positioning mechanism I3 and the movable arm plate positioning mechanism II 4.
In the embodiment, the seat beam positioning bracket 5 is arranged at the center of the base 1 to position the seat beam, and the seat beam supporting seat 6 is arranged at the left side of the seat beam positioning bracket 5 to support the seat beam; two movable arm plate positioning mechanisms I3 are arranged on the left side of the seat beam positioning mechanism 2, two movable arm plate positioning mechanisms II 4 are arranged on the right side of the seat beam positioning mechanism 2, and the two movable arm plates of the seat beam can be positioned, so that the two movable arm plates can be welded and assembled at the same time; the movable arm plate auxiliary positioning mechanism 19 is used for carrying out auxiliary positioning on the movable arm plate and ensuring the stability of the movable arm plate during welding; the boom plate support base 24 is used to support the boom plate.
The first base plate 9 is connected to the base 1 through a connecting bolt, a plurality of groups of connecting threaded holes are formed in the base 1, and the position of the first movable arm plate positioning mechanism 3 can be changed by changing the installation position of the first base plate 9.
When the positioning core shaft is used, the positioning core shaft 7 penetrates into the through hole of the seat beam, then two ends of the positioning core shaft 7 are respectively placed in the two V-shaped positioning grooves 17, the positioning bolt I8 is rotated, the positioning bolt I8 is tightly propped against the seat beam so as to axially position the seat beam, and at the moment, the bottom of the seat beam is just in contact with the seat beam supporting seat 6 so as to be supported; then the movable arm plate is placed between two side plates 21 of the movable arm plate auxiliary positioning mechanism 19, at the moment, one end part of the movable arm plate is positioned on the cushion block 18 and abuts against the baffle 15, the second positioning bolt 16 is rotated to enable the second positioning bolt 16 to tightly push the movable arm plate, the other end part of the movable arm plate is positioned through the T-shaped block 10 and the U-shaped positioning groove 12 on the positioning block 11, the bottom of the movable arm plate is supported by contacting with a movable arm plate supporting seat 24, and the third positioning bolt 23 is rotated to enable the third positioning bolt 23 to tightly push the movable arm plate so as to achieve auxiliary positioning on the movable arm plate; and finally, welding and assembling the seat beam and the movable arm plate.
The middle seat beam realizes positioning under the matching action of the positioning mandrel 7 and the positioning bolt I8; the movable arm plate is positioned under the matching action of the movable arm plate positioning mechanism I, the movable arm plate positioning mechanism II and the movable arm plate auxiliary positioning mechanism 19, the positioning is more reliable, the seat beam or the movable arm plate can be effectively prevented from shaking in the welding process, and the welding quality is ensured.
The utility model discloses utilize the same structure part of unidimensional swing arm as the basis of co-location, fix a position through positioning core axle 7 to the seat beam of all like products, then change corresponding T type piece 10 and locating piece 11 (or the position of adjustment positioning mechanism one) and fix a position the swing arm board through two 16 rotational positioning bolts to the swing arm of unidimensional, not only the benchmark is unified, has reduced the error, has improved suitability and commonality moreover, thereby can reduce equipment input cost.
The foregoing description of the embodiments of the invention has been presented for purposes of illustration and not limitation, and is not intended to be exhaustive or limited to the embodiments disclosed. Many modifications and variations will be apparent to those of ordinary skill in the art without departing from the scope and spirit of the illustrated embodiments.