Background
When the creeper tread is produced, in order to accelerate the production efficiency in batch production, a mold is often used for punching grooves and holes, workers basically put the creeper tread into or out of the mold manually by people during operation, most of the placement positions of the creeper tread are located in the center of the mold, and therefore the creeper tread is very inconvenient to manually take or put parts, accidents are easily caused to happen simultaneously, and therefore the combined mold for punching the slotted holes of the creeper tread is provided.
SUMMERY OF THE UTILITY MODEL
An object of the utility model is to provide a grip-pad slotted hole allies oneself with towards assembling die to solve the problem that proposes among the above-mentioned background art.
In order to achieve the above object, the utility model provides a following technical scheme: a track shoe slotted hole punching combined die comprises a base, wherein a lower die plate is fixedly mounted at the upper end of the base, limiting sliding columns are mounted at four corners of the base, an upper die plate for mounting a cutter is mounted at the upper ends of the limiting sliding columns, nitrogen springs are fixedly mounted on the front sides and the rear sides of the two transverse ends of the lower die plate, an extrusion plate matched with the lower die plate is fixedly mounted at the upper ends of the nitrogen springs, a first sliding groove is formed in the middle of the lower die plate, a placing die plate is slidably mounted in the inner cavity of the first sliding groove, and an ejecting device and a clamping device matched with the placing die plate are mounted on the two transverse side walls of the first sliding groove;
the clamping device comprises a mounting cavity transversely arranged in the lower template and an insertion groove arranged on the upper surface of the lower template, the head end of the mounting cavity is communicated with the first sliding groove, the tail end of the mounting cavity is communicated with the insertion groove, the head end of the mounting cavity is sleeved with a bouncing fixture block matched with the mounting cavity, the cross section of the bouncing fixture block is square, the head end of the bouncing fixture block is clamped with a clamping groove arranged on the side wall of the placing template, the tail end of the bouncing fixture block is screwed with a screw rod, the outer side wall of the screw rod is provided with a torsion spring, the tail end of the screw rod is fixedly provided with a one-way bearing, the outer side wall of the one-way bearing is fixedly provided with a gear, the inner side wall of the insertion groove is spliced with a bar, the lower end of the outer side wall of the bar is provided;
the fixture block comprises a block body, a square cavity is formed in the block body, a first spring is sleeved in an inner cavity of the square cavity, a square sliding block is sleeved in the inner cavity of the square cavity, the inner end of the square sliding block is attached to the first spring, and the outer end of the square sliding block is in threaded connection with the screw rod.
Preferably, the placing template comprises a supporting block, a supporting male die is fixedly mounted on the upper surface of the supporting block, two cross-section T-shaped grooves are vertically formed in the upper surface of the supporting block, a T-shaped inserting block is sleeved in an inner cavity of each cross-section T-shaped groove, and a second spring is sleeved on the outer side wall of each T-shaped inserting block.
Preferably, the popping device comprises a second chute arranged on the side wall of the inner cavity of the first chute, a third spring is sleeved on the inner side wall of the second chute, a sliding block fixedly arranged on the outer side wall of the supporting block is slidably arranged on the inner side wall of the second chute, and the sliding block is attached to the third spring.
Preferably, the stripper plate package rubbing board body, the bottom surface fixed mounting of plate body have with the spacing mould of grip-pad assorted, the upper surface of plate body runs through there is the cutter to pass through the hole, the bottom surface fixed mounting of plate body has two and T shape inserted block upper end extruded extrusion piece mutually.
Preferably, the inner cavity of the first sliding groove is provided with a limiting block, and the bottom surface of the inner cavity of the first sliding groove is vertically provided with two limiting slots matched with the T-shaped inserting block.
Compared with the prior art, the beneficial effects of the utility model are that: the utility model provides a grip-pad slotted hole allies oneself with towards assembling die, the utility model discloses a first spout with place the template cooperation, the messenger places the board and can remove in first spout, simultaneously the utility model discloses a pop-up device and latch device's use, place the template and can be popped out by pop-up device after grip-pad processing, the workman can take off the grip-pad of processing the end, places unprocessed grip-pad, will place the template once more and push into and can process here to place and take out the trouble and the problem that leads to danger easily of part in having avoided the workman hand to stretch into the mould.
Drawings
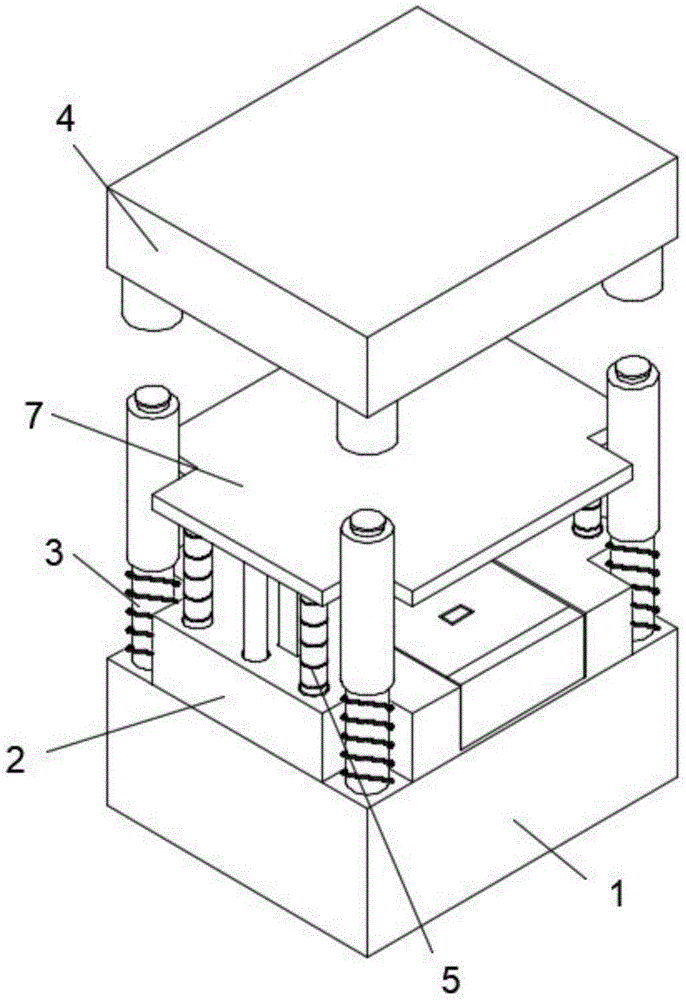
FIG. 1 is a schematic structural view of the present invention;
FIG. 2 is the whole structure diagram of the lower template of the utility model;
FIG. 3 is a schematic view of the structure of the lower template part of the present invention;
FIG. 4 is a schematic structural view of the latch device of the present invention;
FIG. 5 is an enlarged view of point A of FIG. 4 according to the present invention;
FIG. 6 is a schematic view of the point B shown in FIG. 4 according to the present invention;
FIG. 7 is a schematic view of the structure of the bouncing fixture block of the present invention;
FIG. 8 is a schematic view of the placement template of the present invention;
fig. 9 is a schematic diagram of the structure of the extrusion plate of the present invention.
In the figure: 1 base, 2 lower die plate, 3 limit sliding column, 4 upper die plate, 5 nitrogen spring, 6 limit slot, 7 extrusion plate, 71 plate body, 72 limit die, 73 cutter through hole, 74 extrusion block, 8 first chute, 9 placement die plate, 91 supporting block, 92 supporting convex die, 93 section T-shaped slot, 94T-shaped insert block, 95 second spring, 10 ejecting device, 101 second chute, 102 third spring, 103 sliding block, 11 clamping device, 11-1 installation cavity, 11-2 insertion slot, 11-3 bounce clamping block, 11-3a block body, 11-3b square cavity, 11-3c first spring, 11-3d square sliding block, 11-4 clamping slot, 11-5 screw rod, 11-6 torsion spring, 11-7 one-way bearing, 11-8 gear, 11-9 strip rod, 11-10 tooth slot, 12 a limiting block.
Detailed Description
The technical solutions in the embodiments of the present invention will be described clearly and completely with reference to the accompanying drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only some embodiments of the present invention, not all embodiments. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
Referring to fig. 1-9, the present invention provides a technical solution: a track shoe slotted hole punching combined die comprises a base 1, wherein a lower die plate 2 is fixedly installed at the upper end of the base 1, limiting slide columns 3 are installed at four corners of the base 1, an upper die plate 4 for installing a cutter is installed at the upper ends of the limiting slide columns 3, nitrogen springs 5 are fixedly installed on the front sides and the rear sides of the two transverse ends of the lower die plate 2, an extrusion plate 7 matched with the lower die plate 2 is fixedly installed at the upper ends of the nitrogen springs 5, a first sliding groove 8 is formed in the middle of the lower die plate 2, a placing die plate 9 is slidably installed in the inner cavity of the first sliding groove 8, and an ejecting device 10 and a clamping device 11 matched with the placing die plate 9 are installed on two transverse side walls of the first;
the clamping device 11 comprises a mounting cavity 11-1 transversely arranged in the lower template 2 and an insertion groove 11-2 arranged on the upper surface of the lower template 2, the head end of the mounting cavity 11-1 is communicated with the first sliding groove 8, the tail end of the mounting cavity 11-1 is communicated with the insertion groove 11-2, the head end of the mounting cavity 11-1 is sleeved with a bouncing fixture block 11-3 matched with the mounting cavity 11-1, the section of the bouncing fixture block 11-3 is square, the head end of the bouncing fixture block 11-3 is clamped with a clamping groove 11-4 arranged on the side wall of the placing template 9, the tail end of the bouncing fixture block 11-3 is screwed with a screw rod 11-5, the outer side wall of the screw rod 11-5 is provided with a torsion spring 11-6, and the tail end of the screw rod 11-5 is fixedly provided with a, a gear 11-8 is fixedly installed on the outer side wall of the one-way bearing 11-7, a strip-shaped rod 11-9 is inserted into the inner side wall of the insertion groove 11-2, a tooth groove 11-10 meshed with the gear 11-8 is formed in the lower end of the outer side wall of the strip-shaped rod 11-9, and the upper end of the strip-shaped rod 11-9 is fixedly installed on the bottom surface of the extrusion plate 7;
the bouncing fixture block 11-3 comprises a block body 11-3a, a square cavity 11-3b is formed in the block body 11-3a, a first spring 11-3c is sleeved in the inner cavity of the square cavity 11-3b, a square sliding block 11-3d is sleeved in the inner cavity of the square cavity 11-3b, the inner end of the square sliding block 11-3d is attached to the first spring 11-3c, and the outer end of the square sliding block 11-3d is in threaded connection with a screw rod 11-5.
As shown in fig. 1: the lateral direction is a direction from left to right and the longitudinal direction is a direction from front to back.
Spacing traveller 3 comprises cylinder, sleeve pipe and spring, and the cylinder cup joints with the sleeve pipe mutually, and the spring cup joints the lateral wall lower extreme in the main part, and the upper end and the sheathed tube lower extreme of spring laminate mutually, and the cylindrical groove that cup joints mutually is offered for at the bed die to 3 mounting means of here spacing traveller, and the bottom surface in cylindrical groove is fixed to the main part, when pressing down the sleeve pipe, the sleeve pipe can extrude the spring and together get into cylindrical inslot to can carry on spacingly to the cope match-plate pattern 4 and prevent that the cope match-plate pattern from taking place the skew when 4 descends in the cope match-.
The bottom surface of the upper template 4 is fixedly provided with a cutter fixing plate, the bottom surface of the cutter fixing plate is provided with a cutter, four corners of the bottom surface of the upper template are provided with guide sleeves, and the guide sleeves and the sleeves are fixedly arranged.
The structure and the principle of the nitrogen spring 5 are the same as those of the hydraulic rod structure, the nitrogen spring 5 is connected with an external air compression air pump, the air compression air pump can jack up the extrusion plate 7 when supplying air to the nitrogen spring 5, and when the air compression air pump takes back air, the nitrogen spring 5 contracts, and the extrusion plate 7 descends to extrude a part.
One end of the torsion spring 11-6 is fixed on the mounting cavity 11-1, and the other end is fixed on the screw rod 11-5.
When the clamping device 11 is used for pushing the placing template 9 in, the block body 11-3a on the bouncing clamping block 11-3 is retracted into the mounting cavity 11-1 through the action of the first spring 11-3c, when the bouncing clamping block 11-3 is opposite to the clamping groove 11-4, the block body 11-3a is popped out by the first spring 11-3c and inserted into the clamping groove 11-4 to clamp the placing plate 9, when the extrusion plate 7 descends through the action of the nitrogen spring 5, the bar-shaped rod 11-9 is driven to descend, at the moment, through the action of the one-way bearing 11-7, the gear 11-8 is matched with the tooth groove 11-10 to not drive the screw rod 11-5 to rotate, after the part processing is finished, the extrusion plate 7 ascends to drive the bar-shaped rod 11-9 to descend and ascend, the bar-shaped rod 11-9 is meshed with the tooth groove 11-10 through the gear 11-8, the gear 11-8 is driven to rotate, and at the moment, the ratchet wheel inside the one-way bearing 11-7 is clamped, so that the gear 11-8 rotates and simultaneously drives the screw rod 11-5 to rotate, the screw rod 11-5 drives the bouncing block 11-3 to shrink through the effect of the screw connection with the bouncing clamping block 11-3, at the moment, the bouncing clamping block 11-3 is separated from the clamping groove 11-4, the placing template 9 is popped by the popping device 10, when the tooth groove 11-10 on the bar-shaped rod 11-9 is separated from the gear 11-8, the torsion spring 11-6 drives the screw rod 11-5 to restore the original state, and at the moment, the bouncing clamping block 11-3 restores the original state.
Specifically, the placing template 9 comprises a supporting block 91, a supporting male die 92 is fixedly mounted on the upper surface of the supporting block 91, two cross-section T-shaped grooves 93 are vertically formed in the upper surface of the supporting block 91, a T-shaped inserting block 94 is sleeved in an inner cavity of each cross-section T-shaped groove 93, and a second spring 95 is sleeved on the outer side wall of each T-shaped inserting block 94.
The supporting punch 92 matches the shape of the bottom surface of the part while supporting the part.
The cross-section T-shaped groove 93 and the T-shaped block 94 are sleeved together, and when the T-shaped block 94 is pressed, the lower end of the T-shaped block 94 can extend out of the lower end of the T-shaped groove.
Specifically, the pop-up device 10 includes a second chute 101 formed on the side wall of the inner cavity of the first chute 8, a third spring 102 is sleeved on the inner side wall of the second chute 101, a slider 103 fixedly mounted on the outer side wall of the supporting block 91 is slidably mounted on the inner side wall of the second chute 101, and the slider 103 is attached to the third spring 102.
The slide block 103 is slidably mounted in the sliding groove 101 for placing the third spring 102, so that when the supporting block 91 pushes the mold, the third spring 102 is pressed, the compression spring is in a compressed state, and when the placing template 9 is separated from the clamping device 11, the placing template 9 can be ejected by the third spring 102.
Specifically, the extrusion plate 7 includes a plate body 71, a limiting die 72 matched with the track shoe is fixedly mounted on the bottom surface of the plate body 71, a cutter passing hole 73 penetrates through the upper surface of the plate body 71, and two extrusion blocks 74 extruded with the upper end of a T-shaped insert block 94 are fixedly mounted on the bottom surface of the plate body 71.
When the extrusion plate 7 descends, the track shoe is extruded on the support male die 92 through the limiting die 72, and meanwhile, the extrusion block 74 is extruded on the T-shaped insert block 94, so that the T-shaped insert block 94 extends out of the T-shaped groove 93.
Specifically, the inner cavity of the first sliding chute 8 is provided with a limiting block 12, and the bottom surface of the inner cavity of the first sliding chute 8 is vertically provided with two limiting slots 6 matched with the T-shaped inserting blocks 94.
When the T-shaped inserting block 94 extends out of the section T-shaped groove 93, the T-shaped inserting block can enter the limiting slot 6, so that the placing template 9 is prevented from moving accidentally when parts are machined, and the limiting block 12 is used for limiting the placing template 9.
The working principle is as follows: the utility model discloses when using, be in the same place cope match-plate pattern 4 and hydraulic press are fixed, place the part when processing the part on placing template 9, then will place template 9 and push into lower bolster 2, latch device 11 will place template 9 and block this moment, nitrogen spring 5 shrink this moment, stripper plate 7 descends thereupon, extrude the part and push down, then start the press, control cope match-plate pattern 4 drives the cutter and descends and process the part, after processing, cope match-plate pattern 4 is pulled back by the press, start nitrogen spring 5, nitrogen spring 5 lifts stripper plate 7, latch device 11 will remove the joint to placing template 9 this moment, it can be popped out by pop-up device 10 to place template 9, it can to change the part and repeat above-mentioned operation.
Although embodiments of the present invention have been shown and described, it will be appreciated by those skilled in the art that changes, modifications, substitutions and alterations can be made in these embodiments without departing from the principles and spirit of the invention, the scope of which is defined in the appended claims and their equivalents.