CN212169101U - A large-diameter twist drill with double R groove - Google Patents
A large-diameter twist drill with double R groove Download PDFInfo
- Publication number
- CN212169101U CN212169101U CN202020548383.7U CN202020548383U CN212169101U CN 212169101 U CN212169101 U CN 212169101U CN 202020548383 U CN202020548383 U CN 202020548383U CN 212169101 U CN212169101 U CN 212169101U
- Authority
- CN
- China
- Prior art keywords
- drill
- double
- groove
- cutting edges
- chip removal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Drilling Tools (AREA)
Abstract
本实用新型揭示了一种双R槽型的大直径麻花钻,包括钻头主体和钻轴,所述钻头主体对应设置于所述钻轴一侧并为一体式结构设置,所述钻头主体表面设置有两条切削刃,两切削刃呈螺旋形结构分布设置,两切削刃之间分别对应设置有排屑槽,所述切削刃的端部一侧设置有内冷孔,所述钻轴的尾端中部设置有定位槽,所述钻轴在定位槽内设置有两条螺旋结构分布的内冷槽,所述排屑槽内设置有两个R角。本实用新型结构简单、合理、可靠,加工使用方便,通过改变麻花钻的排屑槽槽型来改变排屑方式,从而达到断屑不绕屑的目的,使排屑顺畅。
The utility model discloses a double-R groove type large-diameter twist drill, which comprises a drill bit main body and a drill shaft. There are two cutting edges, the two cutting edges are arranged in a spiral structure, and there are corresponding chip removal grooves between the two cutting edges. The middle part of the end is provided with a positioning groove, the drill shaft is provided with two internal cooling grooves distributed in a spiral structure in the positioning groove, and two R angles are provided in the chip removal groove. The utility model has the advantages of simple, reasonable and reliable structure, convenient processing and use, and the chip removal mode can be changed by changing the chip removal groove shape of the twist drill, so as to achieve the purpose of breaking the chips without wrapping the chips and making the chip removal smooth.
Description
技术领域technical field
本实用新型涉及汽车行业发动机油泵加工用刀具领域,尤其涉及一种双R槽型的大直径麻花钻。The utility model relates to the field of tools for machining engine oil pumps in the automobile industry, in particular to a large-diameter twist drill with double R grooves.
背景技术Background technique
钻头用于粗加工打孔,本文介绍的钻头是加工一个D15的孔,由于客户局限性,没有多余的装刀具的刀塔,导致本孔设计最多只能3支刀具,所以加工底孔的钻头外径不能过小。打底孔钻头过大会有排屑难和加工阻力大等问题,而且加工的材料是韧性好的钢材,不易断屑,更加大了排屑的困难。钻头常常因不断屑问题崩刃,本来钻头可以修磨3次,由于崩刃原因常常用1次就无法修磨了,增加了客户的成本。The drill bit is used for roughing and drilling. The drill bit introduced in this article is to process a D15 hole. Due to customer limitations, there is no extra turret for installing tools, resulting in a maximum of 3 tools for this hole design, so the drill bit for processing bottom holes The outer diameter cannot be too small. If the bottom hole drill is too large, it will cause problems such as difficult chip removal and large processing resistance, and the processed material is a steel with good toughness, which is not easy to break chips, which makes chip removal even more difficult. The drill bit is often chipped due to the problem of continuous chipping. Originally, the drill bit can be ground three times. Due to chipping, it is often unable to be ground after one use, which increases the customer's cost.
实用新型内容Utility model content
本实用新型的目的在于提供一种结构简单、合理、可靠,加工使用方便,通过改变麻花钻的排屑槽槽型来改变排屑方式,从而达到断屑不绕屑的目的,使排屑顺畅的双R槽型的大直径麻花钻。The purpose of the utility model is to provide a simple, reasonable and reliable structure, which is easy to process and use. The chip removal method can be changed by changing the chip removal groove shape of the twist drill, so as to achieve the purpose of breaking the chips without turning the chips around and making the chip removal smooth. Large diameter twist drill with double R geometry.
本实用新型的技术方案是,一种双R槽型的大直径麻花钻,包括钻头主体和钻轴,所述钻头主体对应设置于所述钻轴一侧并为一体式结构设置,所述钻头主体表面设置有两条切削刃,两切削刃呈螺旋形结构分布设置,两切削刃之间分别对应设置有排屑槽,所述切削刃的端部一侧设置有内冷孔,所述钻轴的尾端中部设置有定位槽,所述钻轴在定位槽内设置有两条螺旋结构分布的内冷槽,所述排屑槽内设置有两个R角。The technical scheme of the present invention is that a double-R groove type large-diameter twist drill comprises a drill bit main body and a drill shaft. The surface of the main body is provided with two cutting edges, the two cutting edges are arranged in a spiral structure, and there are corresponding chip removal grooves between the two cutting edges. A positioning groove is arranged in the middle of the tail end of the shaft, the drilling shaft is provided with two internal cooling grooves distributed in a spiral structure in the positioning groove, and two R angles are arranged in the chip removal groove.
在本实用新型一个较佳实施例中,所述钻头主体的直径大小小于钻轴的直径大小。In a preferred embodiment of the present invention, the diameter of the main body of the drill bit is smaller than the diameter of the drill shaft.
在本实用新型一个较佳实施例中,两所述切削刃端部的夹角为140°。In a preferred embodiment of the present invention, the included angle between the ends of the two cutting edges is 140°.
在本实用新型一个较佳实施例中,两所述R角拼接设置于排屑槽内。In a preferred embodiment of the present invention, the two R-angles are spliced and arranged in the chip flute.
在本实用新型一个较佳实施例中,两所述R角分别设置于排屑槽中部两侧。In a preferred embodiment of the present invention, the two R angles are respectively arranged on both sides of the middle of the chip flute.
本实用新型所述为一种双R槽型的大直径麻花钻,本实用新型结构简单、合理、可靠,加工使用方便,通过改变麻花钻的排屑槽槽型来改变排屑方式,从而达到断屑不绕屑的目的,使排屑顺畅。The utility model relates to a large-diameter twist drill with double R grooves. The utility model has a simple, reasonable and reliable structure, and is convenient to process and use. The purpose of breaking the chip without going around the chip makes the chip removal smooth.
附图说明Description of drawings
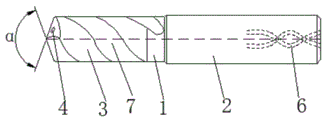
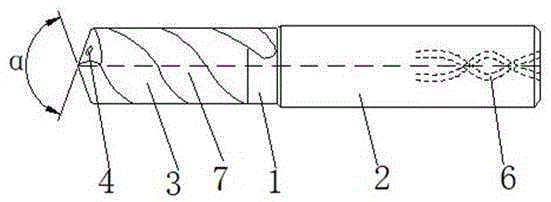
图1为本实用新型双R槽型的大直径麻花钻一较佳实施例中的正视图;1 is a front view in a preferred embodiment of the large-diameter twist drill of the double R groove type of the utility model;
图2为图1的左视图;Fig. 2 is the left side view of Fig. 1;
图3为图1的右视图。FIG. 3 is a right side view of FIG. 1 .
具体实施方式Detailed ways
下面对本实用新型的较佳实施例进行详细阐述,以使本实用新型的优点和特征能更易于被本领域技术人员理解,从而对本实用新型的保护范围做出更为清楚明确的界定。The preferred embodiments of the present invention are described in detail below, so that the advantages and features of the present invention can be more easily understood by those skilled in the art, so as to define the protection scope of the present invention more clearly.
本实用新型所述为一种双R槽型的大直径麻花钻,如图1结合图2-图3所示,包括钻头主体1和钻轴2,钻头主体1对应设置于钻轴2一侧并为一体式结构设置,保证整体结构的强度,钻头主体1的直径大小小于钻轴2的直径大小,方便加工。The utility model is a large-diameter twist drill with double R grooves. As shown in FIG. 1 in conjunction with FIGS. 2 to 3 , it includes a drill bit body 1 and a drill shaft 2 , and the drill bit body 1 is correspondingly arranged on one side of the drill shaft 2 It is set as an integral structure to ensure the strength of the overall structure. The diameter of the drill bit body 1 is smaller than the diameter of the drill shaft 2, which is convenient for processing.
钻头主体1表面设置有两条切削刃3,两切削刃3端部的夹角α为140°,两切削刃3呈螺旋形结构分布设置,根据产品进行适应性加工,切削刃3的端部一侧设置有内冷孔4,便于加工时冷却。The surface of the drill main body 1 is provided with two
钻轴2的尾端中部设置有定位槽5,钻轴2在定位槽5内设置有两条螺旋结构分布的内冷槽6,同样用于对麻花钻在使用过程中起到一个降温冷却的作用。The middle of the rear end of the drill shaft 2 is provided with a
两切削刃3之间分别对应设置有用于排屑的排屑槽7,排屑槽7中部两侧拼接设置有两个R角包括R1和R2,麻花钻在加工中断屑是通过加工的速度使铁屑快速冲击到R2面撞断铁屑,从而使排屑顺畅,由此减少麻花钻的崩刃现象,提高麻花钻的使用寿命。A
本实用新型所述为一种双R槽型的大直径麻花钻,本实用新型结构简单、合理、可靠,加工使用方便,通过改变麻花钻的排屑槽槽型来改变排屑方式,从而达到断屑不绕屑的目的,使排屑顺畅。The utility model relates to a large-diameter twist drill with double R grooves. The utility model has a simple, reasonable and reliable structure, and is convenient to process and use. The purpose of breaking the chip without going around the chip makes the chip removal smooth.
以上所述仅为本实用新型的具体实施方式,但本实用新型的保护范围并不局限于此,任何熟悉本领域的技术人员在本实用新型所揭露的技术范围内,可不经过创造性劳动想到的变化或替换,都应涵盖在本实用新型的保护范围之内。因此,本实用新型的保护范围应该以权利要求书所限定的保护范围为准。The above are only specific embodiments of the present utility model, but the protection scope of the present utility model is not limited to this. Any person skilled in the art can come up with ideas without creative work within the technical scope disclosed by the present utility model. Changes or substitutions should be covered within the protection scope of the present invention. Therefore, the protection scope of the present invention should be based on the protection scope defined by the claims.
Claims (5)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202020548383.7U CN212169101U (en) | 2020-04-15 | 2020-04-15 | A large-diameter twist drill with double R groove |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202020548383.7U CN212169101U (en) | 2020-04-15 | 2020-04-15 | A large-diameter twist drill with double R groove |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN212169101U true CN212169101U (en) | 2020-12-18 |
Family
ID=73770029
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202020548383.7U Expired - Fee Related CN212169101U (en) | 2020-04-15 | 2020-04-15 | A large-diameter twist drill with double R groove |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN212169101U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113770425A (en) * | 2021-09-22 | 2021-12-10 | 辽宁工程技术大学 | Combined twist drill for processing stepped hole with inner chamfer |
-
2020
- 2020-04-15 CN CN202020548383.7U patent/CN212169101U/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113770425A (en) * | 2021-09-22 | 2021-12-10 | 辽宁工程技术大学 | Combined twist drill for processing stepped hole with inner chamfer |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2027957B9 (en) | A strong high performance twist drill | |
| CN103586636B (en) | The processing method of spout and the processing unit (plant) of spout | |
| CN103737090B (en) | A kind of fine finishining rotary cutting tool | |
| CN107262786A (en) | A kind of band stops section step drill and its manufacture method | |
| CN207171033U (en) | A kind of combined type drilling reamer for fine cut shallow bore hole | |
| CN202263964U (en) | Inner cold spiral-hole twist drill | |
| CN205519810U (en) | Special chip removal ladder downwards of steel part bores | |
| CN212094508U (en) | Chip breaking grinding milling drill for drill tip | |
| CN205684788U (en) | A kind of tail stock is with indexable Morse taper shank composite drill | |
| CN107498096A (en) | Combined type drilling reamer for fine cut shallow bore hole | |
| CN103042259A (en) | Inner-cooling stepped drill | |
| CN218983220U (en) | Composite fine boring cutter | |
| CN212169097U (en) | A large R angle step drill for processing stainless steel | |
| CN101700579B (en) | High-precision hole-machining drilling and boring cutter | |
| CN216990021U (en) | A solid carbide deep hole drill | |
| CN205733143U (en) | A kind of three traverse drill reaming step drill | |
| CN203459721U (en) | Ellipsoid drill bit | |
| CN210996695U (en) | Novel step forming reamer for removing annular iron chips of cast blind holes | |
| CN105689765A (en) | Drill bit special for carbon fiber composite | |
| CN108161083A (en) | For the drilling reamer of steering knuckle king pin hole processing | |
| CN201783682U (en) | Drill bit for drilling large length-diameter ratio deep holes | |
| CN105252089A (en) | Precision cutting tool for high-hardness die steel | |
| CN206047127U (en) | A kind of multi-functional lathe tool | |
| CN207464335U (en) | Hard alloy Double-head rotation filing | |
| CN113319351A (en) | Cold cutter in lateral wall processing |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address |
Address after: 215500 10-15 Nanbang Road, Maoqiao Village, Changfu street, Changshu City, Suzhou City, Jiangsu Province Patentee after: Suzhou LEIWANG Intelligent System Co.,Ltd. Address before: 215500 Maoqiao Village, Yushan Town, Changshu City, Suzhou City, Jiangsu Province Patentee before: CHANGSHU LEIWANG ALLOY TOOLS Co.,Ltd. |
|
| CP03 | Change of name, title or address | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20201218 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |