CN211162636U - A welding tool for a thrust rod beam assembly of a tourist vehicle - Google Patents
A welding tool for a thrust rod beam assembly of a tourist vehicle Download PDFInfo
- Publication number
- CN211162636U CN211162636U CN201922194302.8U CN201922194302U CN211162636U CN 211162636 U CN211162636 U CN 211162636U CN 201922194302 U CN201922194302 U CN 201922194302U CN 211162636 U CN211162636 U CN 211162636U
- Authority
- CN
- China
- Prior art keywords
- thrust rod
- positioning plate
- plate
- beam assembly
- workbench
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003466 welding Methods 0.000 title claims abstract description 38
- 230000003014 reinforcing effect Effects 0.000 claims description 28
- 238000005452 bending Methods 0.000 claims description 3
- 238000005728 strengthening Methods 0.000 claims 2
- 239000000463 material Substances 0.000 abstract description 6
- 239000002699 waste material Substances 0.000 abstract description 2
- 238000007493 shaping process Methods 0.000 abstract 1
- 230000002787 reinforcement Effects 0.000 description 9
- 238000004519 manufacturing process Methods 0.000 description 3
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000003698 laser cutting Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
Images


Landscapes
- Butt Welding And Welding Of Specific Article (AREA)
Abstract
Description
技术领域technical field
本实用新型涉及车辆零部件焊接工装领域,特别是涉及一种旅游车简易推力杆横梁总成的高精度焊接工装。The utility model relates to the field of welding tooling for vehicle parts, in particular to a high-precision welding tooling for a simple thrust rod beam assembly of a tourist vehicle.
背景技术Background technique
旅游车推力杆横梁总成由方管横梁、推力杆座垫块、4块推力杆支座加强板焊接而成,推力杆横梁总成结构复杂,制作繁琐,目前制作采用的人工测量定位,即对推力杆横梁总成按照图纸,用卷尺进行定位,手工进行焊接,耗时长、准确性差、稳定性差。The thrust rod beam assembly of the tourist car is welded by the square tube beam, the thrust rod seat cushion block, and the 4 thrust rod support reinforcement plates. The thrust rod beam assembly is complicated in structure and complicated in production. Positioning the thrust rod beam assembly with a tape measure according to the drawing and welding by hand is time-consuming, poor in accuracy and poor in stability.
实用新型内容Utility model content
为解决上述旅游车推力杆横梁总成的定位焊接的技术问题,本实用新型提供一种旅游车推力杆横梁总成焊接工装。In order to solve the above-mentioned technical problem of the positioning welding of the thrust rod beam assembly of the tourist vehicle, the utility model provides a welding tool for the thrust rod beam assembly of the tourist vehicle.
为实现上述目的,本实用新型采用了以下技术方案:To achieve the above object, the utility model adopts the following technical solutions:
一种旅游车推力杆横梁总成焊接工装,用于将方管横梁、两推力杆座垫块和两推力杆支座加强板焊接在一起,包括工作台,工作台上安装有第一定位板、第二定位板和至少两个支撑座,第一定位板和第二定位板垂直于工作台,第一定位板位于第二定位板左方,各支撑座位于第二定位板右方,各支撑座沿左右方向间隔排列,方管横梁放置在支撑座上时,支撑座夹持方管横梁的前后两侧,第二定位板上设有让位通孔,方管横梁左端穿过让位通孔并抵接至第一定位板以就位,第二定位板上端朝右设有两个定位销,两定位销等高,每一定位销穿过一推力杆座垫块和一推力杆支座加强板,两推力杆支座加强板的前端抵接第二定位板,两推力杆支座加强板分别位于方管横梁的前后两侧并贴紧方管横梁。The utility model relates to a welding tool for a thrust rod cross beam assembly of a tourist vehicle, which is used for welding a square tube cross beam, two thrust rod seat cushion blocks and two thrust rod support reinforcing plates, and comprises a workbench on which a first positioning plate is installed. , a second positioning plate and at least two support seats, the first positioning plate and the second positioning plate are perpendicular to the workbench, the first positioning plate is located on the left of the second positioning plate, each support seat is located on the right of the second positioning plate, each The support bases are arranged at intervals along the left and right directions. When the square tube beam is placed on the support base, the support base clamps the front and rear sides of the square tube beam. The second positioning plate is provided with a through hole to give way, and the left end of the square tube beam passes through the space. The through hole is abutted to the first positioning plate to be in place. The upper end of the second positioning plate is provided with two positioning pins facing the right. The two positioning pins are of the same height. Each positioning pin passes through a thrust rod seat cushion block and a thrust rod The front end of the two thrust rod support reinforcing plates abuts the second positioning plate, and the two thrust rod support reinforcing plates are respectively located on the front and rear sides of the square tube beam and are closely attached to the square tube beam.
进一步,所述支撑座包括水平置于工作台上的加强管和分别竖直固定在加强管前后两侧的前侧板和后侧板,前侧板和后侧板之间的间距等于方管横梁的宽度。Further, the support base includes a reinforcing tube horizontally placed on the workbench and a front side plate and a rear side plate vertically fixed on the front and rear sides of the reinforcing tube respectively, and the distance between the front side plate and the rear side plate is equal to the square tube. The width of the beam.
进一步,所述前侧板和后侧板与加强管焊接连接,加强管为方管。Further, the front side plate and the rear side plate are welded and connected with a reinforcing pipe, and the reinforcing pipe is a square pipe.
进一步,所述第一定位板的左侧焊接有两个加强筋,加强筋与工作台焊接。Further, two reinforcing ribs are welded on the left side of the first positioning plate, and the reinforcing ribs are welded with the worktable.
进一步,所述第二定位板的左侧焊接有两个加强筋,加强筋与工作台焊接。Further, two reinforcing ribs are welded on the left side of the second positioning plate, and the reinforcing ribs are welded with the worktable.
进一步,所述工作台由一平板和位于该平板下方支撑该平板的两块立板组成。Further, the workbench is composed of a flat plate and two vertical plates positioned under the flat plate to support the flat plate.
进一步,所述工作台由一平板在左右两端向下弯折90°而成。Further, the worktable is formed by bending a flat plate downward at 90° at the left and right ends.
进一步,所述支撑座的数量为三个,三个支撑座分别支撑方管横梁的左右两端和中间。Further, the number of the support bases is three, and the three support bases respectively support the left and right ends and the middle of the square tube beam.
进一步,所述第一定位板、第二定位板和各支撑座通过焊接固定在工作台上。Further, the first positioning plate, the second positioning plate and each support seat are fixed on the workbench by welding.
与现有技术相比,本实用新型具有以下优点:Compared with the prior art, the utility model has the following advantages:
该旅游车推力杆横梁总成焊接工装结构简单,材料成本低,使用寿命长,该工装的操作简单,在保证推力杆横梁总成精度的同时,还能够提升推力杆横梁总成的制作效率.节省时间并减少后期返工,可靠性好,有效的避免了人力、物力的过多浪费。The welding tooling for the thrust rod beam assembly of the tourist car has a simple structure, low material cost, long service life, and simple operation of the tooling, which can improve the production efficiency of the thrust rod beam assembly while ensuring the accuracy of the thrust rod beam assembly. Save time and reduce later rework, good reliability, and effectively avoid excessive waste of manpower and material resources.
附图说明Description of drawings
图1是旅游车推力杆横梁总成的部分结构装配图之一;Figure 1 is one of the partial structural assembly drawings of the thrust rod beam assembly of the tourist vehicle;
图2是旅游车推力杆横梁总成的部分结构装配图之二;Figure 2 is the second part of the structural assembly drawing of the thrust rod beam assembly of the tourist vehicle;
图3是旅游车推力杆横梁总成焊接工装的立体图之一;Figure 3 is one of the perspective views of the welding tooling of the thrust rod beam assembly of the tourist car;
图4是旅游车推力杆横梁总成焊接工装的立体图之二;Figure 4 is the second perspective view of the welding tooling of the thrust rod beam assembly of the tourist vehicle;
图5是旅游车推力杆横梁总成和焊接工装的装配图。Figure 5 is an assembly drawing of the travel car thrust rod beam assembly and welding tooling.
具体实施方式Detailed ways
为进一步说明各实施例,本实用新型提供有附图。这些附图为本实用新型揭露内容的一部分,其主要用以说明实施例,并可配合说明书的相关描述来解释实施例的运作原理。配合参考这些内容,本领域普通技术人员应能理解其他可能的实施方式以及本实用新型的优点。图中的组件并未按比例绘制,而类似的组件符号通常用来表示类似的组件。To further illustrate the various embodiments, the present invention provides accompanying drawings. These drawings are a part of the disclosure of the present invention, which are mainly used to illustrate the embodiments, and can be combined with the relevant description of the specification to explain the operation principles of the embodiments. With reference to these contents, those of ordinary skill in the art should be able to understand other possible embodiments and the advantages of the present invention. Components in the figures are not drawn to scale, and similar component symbols are often used to represent similar components.
在本实用新型的描述中,需要理解的是,术语“宽度”、“上”、“下”、“前”、“后”、“左”、“右”、“竖直”、“水平”等指示的方位或位置关系为基于附图所示的方位或位置关系,仅是为了便于描述本实用新型和简化描述,而不是指示或暗示所指的装置或元件必须具有特定的方位、以特定的方位构造和操作,因此不能理解为对本实用新型的限制。In the description of the present invention, it should be understood that the terms "width", "upper", "lower", "front", "rear", "left", "right", "vertical", "horizontal" The orientation or positional relationship indicated by etc. is based on the orientation or positional relationship shown in the accompanying drawings, which is only for the convenience of describing the present invention and simplifying the description, rather than indicating or implying that the referred device or element must have a specific orientation, with a specific orientation. Therefore, it should not be construed as a limitation on the present invention.
图1和图2是一种旅游车推力杆横梁总成的部分结构装配图,包括一个方管横梁1、两个推力杆座垫块2和两个推力杆支座加强板3。本实施例公开一种旅游车推力杆横梁总成焊接工装,用于将方管横梁1、两推力杆座垫块2和两推力杆支座加强板3焊接在一起形成图1所示的推力杆横梁总成半成品。推力杆横梁总成焊接工装整体拼接成型,推力杆横梁总成焊接工装是依据与推力杆横梁总成形状设计而成的,主要运用的是逆向思维—将推力杆横梁总成反着制作,只需要将推力杆横梁总成的物料依次放到工装对应的位置上,然后焊接固定即可,以下介绍该工装的具体结构。1 and 2 are partial structural assembly drawings of a thrust rod beam assembly of a tourist vehicle, including a
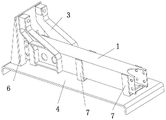
请参阅图3至图5,该焊接工装包括工作台4,工作台4上安装有第一定位板5、第二定位板6和至少两个支撑座7,第一定位板5和第二定位板6垂直于工作台4,第一定位板5位于第二定位板6左方,各支撑座7位于第二定位板6右方,各支撑座7沿左右方向间隔排列,方管横梁1放置在支撑座7上时,支撑座7夹持方管横梁1的前后两侧,第二定位板6上设有让位通孔,方管横梁1左端穿过让位通孔并抵接至第一定位板5以就位;第二定位板6上端朝右设有两个定位销8,两定位销8等高。Please refer to FIG. 3 to FIG. 5 , the welding tool includes a
如图1和图2所示,推力杆座垫块2设有一通孔,推力杆支座加强板3上端设有与推力杆座垫块2上的通孔相对应的通孔,将推力杆座垫块2的通孔和推力杆支座加强板3上的通孔对准,每一定位销8穿过一推力杆座垫块2和一推力杆支座加强板3,两推力杆支座加强板3的前端抵接第二定位板6,两推力杆支座加强板3分别位于方管横梁1的前后两侧并贴紧方管横梁1,如此实现方管横梁1、两推力杆座垫块2和两推力杆支座加强板3的就位。As shown in Figures 1 and 2, the thrust rod
在本实施例中,支撑座7的数量为三个,三个支撑座7分别支撑方管横梁1的左右两端和中间。In this embodiment, the number of the
支撑座7的结构可以有多种,在本实施例中,如图4所示,支撑座7包括水平置于工作台4上的加强管71和分别竖直固定在加强管71前后两侧的前侧板72和后侧板73,前侧板72和后侧板73之间的间距等于方管横梁1的宽度。The
前侧板72和后侧板73可以采用焊接、螺纹连接等方式实现与加强管71的连接,本实施中优选采用焊接,并且加强管71优选为方管,在满足强度要求的基础上,减轻整个工装的重量。The
如图4所示,第一定位板5的左侧焊接有两个加强筋9,第二定位板6的左侧焊接有两个加强筋9,各加强筋9与工作台4焊接以支撑第一定位板5或第二定位板6。As shown in FIG. 4 , two reinforcing
工作台4由一平板和位于该平板下方支撑该平板的两块立板组成,如此方便采用叉车等工具搬运工作台4。优选地,工作台4由一平板在左右两端向下弯折90°而成,一体成型有利于简化制造工序。The
在本实施例中,第一定位板5、第二定位板6和各支撑座7通过焊接固定在工作台4上。第一定位板5采用激光下料,减小误差,保证准确性,稳定性。In this embodiment, the
根据技术要求,制作出旅游车推力杆支座的定位工装,后续对旅游车推力杆横梁总成制作焊接工装,将推力杆横梁总成的物料依次放到焊接工装对应的位置上,然后焊接固定即可。According to the technical requirements, the positioning tooling for the thrust rod support of the tourist vehicle is made, and the welding tooling is made for the thrust rod beam assembly of the tourist vehicle. The materials of the thrust rod beam assembly are placed in the corresponding position of the welding tooling, and then welded and fixed. That's it.
尽管结合优选实施方案具体展示和介绍了本实用新型,但所属领域的技术人员应该明白,在不脱离所附权利要求书所限定的本实用新型的精神和范围内,在形式上和细节上可以对本实用新型做出各种变化,均为本实用新型的保护范围。Although the present invention has been specifically shown and described in conjunction with preferred embodiments, it will be understood by those skilled in the art that changes in form and detail may be made without departing from the spirit and scope of the present invention as defined by the appended claims. Various changes are made to the present utility model, which are all within the protection scope of the present utility model.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922194302.8U CN211162636U (en) | 2019-12-10 | 2019-12-10 | A welding tool for a thrust rod beam assembly of a tourist vehicle |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922194302.8U CN211162636U (en) | 2019-12-10 | 2019-12-10 | A welding tool for a thrust rod beam assembly of a tourist vehicle |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211162636U true CN211162636U (en) | 2020-08-04 |
Family
ID=71817801
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201922194302.8U Active CN211162636U (en) | 2019-12-10 | 2019-12-10 | A welding tool for a thrust rod beam assembly of a tourist vehicle |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211162636U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112719756A (en) * | 2020-12-31 | 2021-04-30 | 真木农业设备(安徽)有限公司 | Water tank support mounting tool |
-
2019
- 2019-12-10 CN CN201922194302.8U patent/CN211162636U/en active Active
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112719756A (en) * | 2020-12-31 | 2021-04-30 | 真木农业设备(安徽)有限公司 | Water tank support mounting tool |
| CN112719756B (en) * | 2020-12-31 | 2023-11-14 | 真木农业设备(安徽)有限公司 | Water tank bracket mounting tool |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN101804538A (en) | Process apparatus for fixedly welding camber profile frame and positioning method thereof | |
| CN110816778B (en) | A construction method of a ship's lap-joint trough bulkhead | |
| CN106799554B (en) | A special welding fixture system for gas spring type full load frame assembly | |
| CN201792157U (en) | Universal motorcycle frame welding fixture | |
| CN213257878U (en) | Aeroengine packing box support welding frock | |
| CN221064983U (en) | Convenient assembly device for electroslag welding baffle lining strip | |
| CN215469195U (en) | Bus distance rod bottom end rail assembly welding frock | |
| CN216730266U (en) | Sleeper beam assembly welding locating rack and assembly welding device | |
| CN111774616B (en) | Three-dimensional projection auxiliary assembly fixture | |
| CN113941813A (en) | Sleeper beam assembly welding positioning frame, assembly welding device and method | |
| CN223406300U (en) | Packing box assembly welding frock | |
| CN212265026U (en) | Left control handle pre-welding device of mixer truck | |
| CN214641327U (en) | Improved generation connecting rod welding frock | |
| CN219852892U (en) | Welding appurtenance | |
| CN222986064U (en) | Bearing arm tool | |
| CN223932961U (en) | Welding and assembling jig for forklift mast cross beam and forklift mast cross beam | |
| CN206502048U (en) | Clamp and aircraft assembly fixture | |
| CN220515890U (en) | Welding frock | |
| CN219746770U (en) | Auxiliary assembly jig for framework in bogie | |
| CN223301168U (en) | Frame welding frock | |
| CN215413497U (en) | Device for detecting coaxiality and size of inner frame and outer frame of scissor ascending truck | |
| CN215318645U (en) | Foundation equipment connecting bolt positioner | |
| CN222958398U (en) | Forward type fork truck front-shifting frame location splicing apparatus | |
| CN217142881U (en) | Welding positioning device | |
| CN222767606U (en) | Isolation transformer box bracket welding tooling |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP02 | Change in the address of a patent holder | ||
| CP02 | Change in the address of a patent holder |
Address after: No.12, Longjun Road, Taishang investment zone, Zhangzhou City, Fujian Province Patentee after: ZHANGZHOU CHANGLONG AUTOMOBILE ACCESSORY Co.,Ltd. Address before: 363000 Ganglong Automobile Industrial Park, Longhai City, Zhangzhou City, Fujian Province (west of Longjun Road) Patentee before: ZHANGZHOU CHANGLONG AUTOMOBILE ACCESSORY Co.,Ltd. |