CN210671982U - Rice Cake Forming Machine - Google Patents
Rice Cake Forming Machine Download PDFInfo
- Publication number
- CN210671982U CN210671982U CN201921258180.8U CN201921258180U CN210671982U CN 210671982 U CN210671982 U CN 210671982U CN 201921258180 U CN201921258180 U CN 201921258180U CN 210671982 U CN210671982 U CN 210671982U
- Authority
- CN
- China
- Prior art keywords
- die
- carriage
- conveyor belt
- cutting
- moulding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Landscapes
- Cereal-Derived Products (AREA)
Abstract
本实用新型公开了一种米饼成型机,沿料的运动方向,机架设有料斗、拨辊、挤压装置、切割装置、推料装置和成型装置,机架上还设有水平设置的料斗传送带、切断传送带和成型传送带,料斗位于料斗传送带的上方,拨辊位于料斗传送带下料端的上方,挤压装置的进料口位于料斗传送带下料端的下方,挤压装置的出料口位于切断传送带上料端的上方,切割装置和推料装置均位于切断传送带的上方,成型传送带的上料端与切断传送带的下料端相对应,成型装置位于成型传送带的上方。整个米饼的生产过程中,完全是自动的,实现了米饼的自动化生产,大大提高了生产效率,成本低,且米饼不会黏在模具上,不需要抠米饼,省时省力,降低了工作人员的负担。
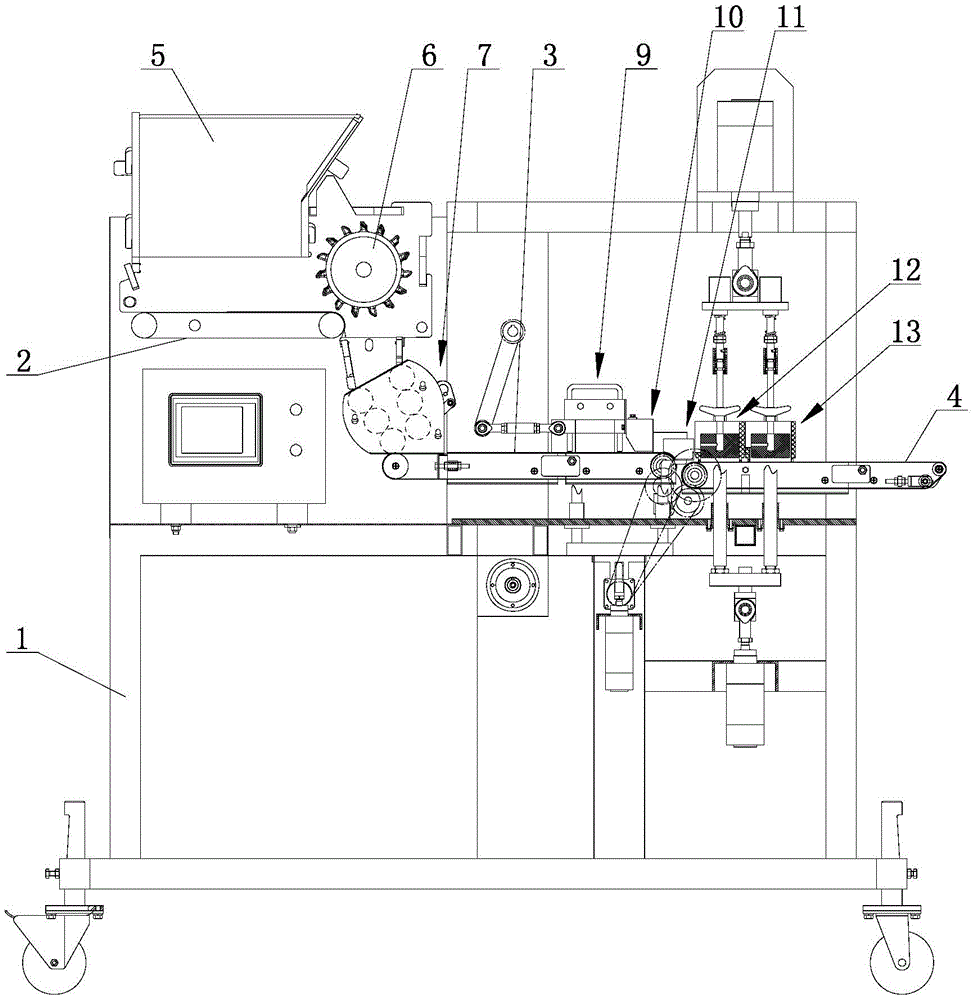
The utility model discloses a rice cake forming machine. Along the moving direction of the material, a frame is provided with a hopper, a dial roller, a pressing device, a cutting device, a pushing device and a forming device, and a horizontally arranged hopper is also arranged on the frame. Conveyor belt, cutting conveyor belt and forming conveyor belt, the hopper is located above the hopper conveyor belt, the dial roller is located above the feeding end of the hopper conveyor belt, the feeding port of the extrusion device is located below the feeding end of the hopper conveyor belt, and the discharging port of the extrusion device is located on the cutting conveyor belt Above the feeding end, the cutting device and the pushing device are located above the cutting conveyor belt, the feeding end of the forming conveyor belt corresponds to the discharging end of the cutting conveyor belt, and the forming device is located above the forming conveyor belt. The whole production process of rice cakes is completely automatic, which realizes the automatic production of rice cakes, greatly improves the production efficiency, low cost, and the rice cakes will not stick to the mold, so there is no need to pull the rice cakes, saving time and effort, Reduce the burden on staff.
Description
技术领域technical field
本实用新型涉及米饼成型机技术领域。The utility model relates to the technical field of rice cake forming machines.
背景技术Background technique
米饼是一种以大米为主要原料,压胚成型的一种食品,可以作为糕点、休闲食品,也可以作为主要的快餐主食。目前,米饼一般是通过手工、滚压方式制作而成,这种方式效率低,而且容易黏在模具上,需要人工把米饼取下来,自动化程度低。Rice cake is a kind of food that uses rice as the main raw material and is formed by pressing embryos. It can be used as a cake, a snack food, or a main fast food staple. At present, rice cakes are generally made by hand and rolling. This method is inefficient, and it is easy to stick to the mold. It needs to be manually removed, and the degree of automation is low.
发明内容SUMMARY OF THE INVENTION
针对上述不足,本实用新型所要解决的技术问题是:提供一种全自动化米饼成型机,以提高米饼生产效率。In view of the above deficiencies, the technical problem to be solved by the present invention is to provide a fully automatic rice cake forming machine to improve the production efficiency of rice cakes.
为解决上述技术问题,本实用新型的技术方案是:For solving the above-mentioned technical problems, the technical scheme of the present utility model is:
一种米饼成型机,包括:机架,沿料的运动方向,所述机架设有料斗、拨辊、挤压装置、切割装置、推料装置和成型装置,所述机架上还设有水平的料斗传送带、切断传送带和成型传送带,A rice cake forming machine, comprising: a frame, along the moving direction of the material, the frame is provided with a hopper, a dial roller, a pressing device, a cutting device, a pushing device and a forming device, and the frame is further provided with Horizontal hopper conveyors, cut-off conveyors and forming conveyors,
所述料斗位于所述料斗传送带的上方,所述拨辊位于所述料斗传送带下料端的上方,所述挤压装置的进料口位于所述料斗传送带下料端的下方,所述挤压装置的出料口位于所述切断传送带上料端的上方,所述切割装置和所述推料装置均位于所述切断传送带的上方,所述成型传送带的上料端与所述切断传送带的下料端相对应,所述成型装置位于所述成型传送带的上方。The hopper is located above the conveyor belt of the hopper, the dial roller is located above the feeding end of the conveyor belt of the hopper, the feeding port of the extrusion device is located below the feeding end of the conveyor belt of the hopper, and the The discharge port is located above the feeding end of the cutting conveyor belt, the cutting device and the pushing device are both located above the cutting conveyor belt, and the feeding end of the forming conveyor belt is the same as the feeding end of the cutting conveyor belt. Correspondingly, the forming device is located above the forming conveyor.
优选地,所述挤压装置包括若干对沿料的运动方向顺次设置的挤压辊,每一对中的两个所述挤压辊间隔设置,且每一对中的两个所述挤压辊的间距逐渐变小。Preferably, the pressing device comprises several pairs of pressing rollers arranged in sequence along the moving direction of the material, two of the pressing rollers in each pair are arranged at intervals, and two of the pressing rollers in each pair are arranged at intervals. The pitch of the pressing rollers gradually becomes smaller.
优选地,所述挤压辊设有三对,沿料的运动方向,三对所述挤压辊分别为第一上挤压辊和第一下挤压辊、第二上挤压辊和第二下挤压辊、第三上挤压辊和第三下挤压辊,所述第二上挤压辊和所述第二下挤压辊之间间距、所述第三上挤压辊和所述第三下挤压辊之间间距分别通过间距调节装置调节;Preferably, there are three pairs of the squeeze rollers, and along the moving direction of the material, the three pairs of the squeeze rollers are the first upper squeeze roller and the first lower squeeze roller, the second upper squeeze roller and the second squeeze roller respectively. The lower squeezing roll, the third upper squeezing roll and the third lower squeezing roll, the distance between the second upper squeezing roll and the second lower squeezing roll, the third upper squeezing roll and the The spacing between the third lower extrusion rollers is adjusted by the spacing adjusting device;
所述间距调节装置包括调节板、中间连杆和轴摆臂,所述调节板的第一端转动于所述第一上挤压辊的端部,所述调节板的第二端与所述中间连杆的第一端铰接,所述中间连杆的第二端与所述轴摆臂的第一端铰接,所述轴摆臂的第二端固定连接有摆臂轴,所述第二上挤压辊和所述第三上挤压辊转动安装于所述调节板上;The distance adjustment device includes an adjustment plate, an intermediate link and a shaft swing arm, the first end of the adjustment plate rotates on the end of the first upper pressing roller, and the second end of the adjustment plate The first end of the intermediate link is hinged, the second end of the intermediate link is hinged with the first end of the axle swing arm, the second end of the axle swing arm is fixedly connected with a swing arm shaft, the second The upper squeezing roller and the third upper squeezing roller are rotatably mounted on the regulating plate;
或者,所述间距调节装置包括调节板、中间连杆和轴摆臂,所述调节板的第一端转动于所述第一下挤压辊的端部,所述调节板的第二端与所述中间连杆的第一端铰接,所述中间连杆的第二端与所述轴摆臂的第一端铰接,所述轴摆臂的第二端固定连接有摆臂轴,所述第二下挤压辊和所述第三下挤压辊转动安装于所述调节板上。Or, the distance adjusting device includes an adjusting plate, an intermediate link and a shaft swing arm, the first end of the adjusting plate rotates on the end of the first lower pressing roller, and the second end of the adjusting plate is connected to the end of the first lower pressing roller. The first end of the intermediate link is hinged, the second end of the intermediate link is hinged with the first end of the shaft swing arm, the second end of the shaft swing arm is fixedly connected with a swing arm shaft, and the The second lower squeezing roller and the third lower squeezing roller are rotatably mounted on the regulating plate.
优选地,所述切断传送带的上方设有饼带规整装置,所述饼带规整装置位于所述挤压装置和所述切割装置之间,所述饼带规整装置包括固定设置的安装架,所述安装架上固定设有两根间隔平行的导条,所述导条沿所述切断传送带的长度方向设置。Preferably, above the cutting conveyor belt is provided with a cake belt regulating device, the cake belt regulating device is located between the pressing device and the cutting device, and the cake belt regulating device includes a fixed installation frame, so Two parallel guide bars are fixed on the mounting frame, and the guide bars are arranged along the length direction of the cutting conveyor belt.
优选地,所述切割装置包括沿所述切断传送带宽度方向设置的滑架,所述滑架的两端分别固定连接有托架,所述托架连接于连接板,每个所述连接板分别连接有滑架升降机构,所述滑架设有切断刀和两套分别位于所述滑架两端的割分机构,所述切断刀沿所述切断传送带的宽度方向设置。Preferably, the cutting device includes a carriage arranged along the width direction of the cutting conveyor, two ends of the carriage are respectively fixedly connected with brackets, the brackets are connected to connecting plates, each of the connecting plates is respectively A carriage lifting mechanism is connected, the carriage is provided with a cutting knife and two sets of dividing mechanisms respectively located at both ends of the carriage, and the cutting knives are arranged along the width direction of the cutting conveyor belt.
优选地,所述滑架升降机构包括滑架举升缸、滑架举升梁、滑架直线轴承和滑架举升轴,所述滑架举升缸与所述滑架举升梁之间铰接连接,所述滑架举升轴的下端与所述滑架举升梁固定,所述滑架举升轴的上端与所述连接板固定,所述滑架举升轴滑动设于所述滑架直线轴承内,所述滑架直线轴承固定于所述机架。Preferably, the carriage lifting mechanism includes a carriage lifting cylinder, a carriage lifting beam, a carriage linear bearing and a carriage lifting shaft, and the gap between the carriage lifting cylinder and the carriage lifting beam is Hinged connection, the lower end of the carriage lifting shaft is fixed with the carriage lifting beam, the upper end of the carriage lifting shaft is fixed with the connecting plate, and the carriage lifting shaft is slidably arranged on the In the carriage linear bearing, the carriage linear bearing is fixed to the frame.
优选地,所述割分机构包括固定于所述滑架且沿所述切断传送带宽度方向的分隔刀导轨,所述分隔刀导轨滑动连接有至少一个滑块,每个滑块固定有一个分隔刀,所述分隔刀沿所述切断传送带的长度方向延伸,每个所述滑块均固定连接于驱动杆,所述驱动杆端部转动连接有滚子,所述滚子设于平面凸轮的滑槽内,所述滑槽与所述切断传送带的长度方向之间夹有锐角,所述滑架连接有用于让所述滑架沿所述切断传送带长度方向往复运动的往复驱动机构;Preferably, the dividing mechanism includes a dividing knife guide rail fixed on the carriage and along the width direction of the cutting conveyor belt, the dividing knife guide rail is slidably connected with at least one sliding block, and each sliding block is fixed with a dividing knife , the dividing knife extends along the length direction of the cutting conveyor belt, each sliding block is fixedly connected to a driving rod, and the end of the driving rod is rotatably connected with a roller, and the roller is arranged on the sliding block of the plane cam. In the groove, there is an acute angle between the chute and the length direction of the cutting conveyor belt, and the carriage is connected with a reciprocating drive mechanism for reciprocating the carriage along the length direction of the cutting conveyor belt;
所述往复驱动机构包括滑架导轨、摆臂和连接杆,滑架导轨固定于所述连接板,所述滑架导轨沿所述切断传送带的长度方向设置,所述托架滑动于所述滑架导轨,所述连接杆的一端与所述滑架铰接,所述连接杆的另一端与所述摆臂的一端铰接,所述摆臂的另一端固定连接有摆臂轴,所述摆臂轴由电机驱动。The reciprocating drive mechanism includes a carriage guide rail, a swing arm and a connecting rod, the carriage guide rail is fixed on the connecting plate, the carriage guide rail is arranged along the length direction of the cutting conveyor belt, and the bracket slides on the sliding frame. One end of the connecting rod is hinged with the carriage, the other end of the connecting rod is hinged with one end of the swing arm, the other end of the swing arm is fixedly connected with a swing arm shaft, and the swing arm The shaft is driven by a motor.
优选地,所述推料装置包括推料安装板,所述推料安装板固定于所述滑架,所述推料安装板固定有沿所述切断传送带宽度方向均布的推料板,所述推料板的数目与所述分隔刀的数目一致。Preferably, the pushing device includes a pushing mounting plate, the pushing mounting plate is fixed on the sliding frame, and the pushing mounting plate is fixed with pushing plates uniformly distributed along the width direction of the cutting conveyor belt, so The number of the pushing plates is the same as the number of the separating knives.
优选地,所述切断传送带和所述成型传送带之间设有分隔装置,所述分隔装置包括沿所述切断传送带宽度方向设置的分隔安装板,所述分隔安装板上固定设有沿所述切断传送带宽度方向均布的分隔板,相邻的所述分隔板之间间隔形成过料通道,所述过料通道与所述推料板的位置和数目一一对应。Preferably, a separation device is provided between the cutting conveyor belt and the forming conveyor belt, and the separation device includes a separation installation plate arranged along the width direction of the cutting conveyor belt, and the separation installation plate is fixedly provided with a separation plate along the cutting conveyor belt. Separation plates that are uniformly distributed in the width direction of the conveyor belt, and passing channels are formed at intervals between the adjacent separation plates, and the positions and numbers of the passing channels correspond to the positions and numbers of the pushing plates one-to-one.
优选地,所述成型装置包括初成型模具和终成型模具,所述初成型模具和所述终成型模具的位置和数目与所述过料通道一一对应,每个所述初成型模具和每个所述终成型模具均包括中空的模具和在所述模具内上下运动的压模,所述模具固定于模具板,所述模具板连接有模具升降机构,所述压模连接有压模升降机构;Preferably, the forming device includes a preliminary forming mold and a final forming mold, the positions and numbers of the preliminary forming mold and the final forming mold correspond to the material feeding passages one-to-one, and each preliminary forming mold And each of the final forming molds includes a hollow mold and a press mold that moves up and down in the mold, the mold is fixed to a mold plate, and the mold plate is connected with a mold lifting mechanism, and the press mold is connected with a Die lifting mechanism;
所述模具升降机构包括模具伸缩缸、模具举升梁、模具直线轴承和模具举升轴,所述模具伸缩缸与所述模具举升梁铰接,所述模具举升轴的下端固定于所述模具举升梁,所述模具举升轴的上端与所述模具板固定连接,所述模具举升轴滑动于所述模具直线轴承内;The mold lifting mechanism includes a mold telescopic cylinder, a mold lifting beam, a mold linear bearing and a mold lifting shaft, the mold telescopic cylinder is hinged with the mold lifting beam, and the lower end of the mold lifting shaft is fixed to the mold lifting shaft. a die lift beam, the upper end of the die lift shaft is fixedly connected with the die plate, and the die lift shaft slides in the die linear bearing;
所述压模升降机构包括压模伸缩缸、压模举升梁、压模举升轴、压模直线轴承和压模连接轴,所述压模伸缩缸与所述压模举升梁铰接,所述压模举升轴与所述压模举升梁固定,所述压模举升轴滑动于所述压模直线轴承,所述压模直线轴承固定于所述机架,所述压模连接轴的下端与所述压模固定连接,所述压模连接轴的上端固定连接于所述压模举升梁,每个所述压模均固定连接有一根所述压模举升轴。The press die lifting mechanism includes a press die telescopic cylinder, a press die lift beam, a press die lift shaft, a press die linear bearing and a press die connecting shaft, and the press die telescopic cylinder is hinged with the press die lift beam, The die lift shaft is fixed with the die lift beam, the die lift shaft slides on the die linear bearing, the die linear bearing is fixed on the frame, and the die The lower end of the connecting shaft is fixedly connected to the die, the upper end of the connecting shaft of the die is fixedly connected to the die lifting beam, and each of the die is fixedly connected with a die lifting shaft.
采用了上述技术方案后,本实用新型的有益效果是:After adopting the above-mentioned technical scheme, the beneficial effects of the present utility model are:
制取米饼时,将熟化的米饭倒入料斗,由料斗传送带输送至拨辊处,拨辊把米饭打松并轴向分布均匀,送入挤压装置,米饭由挤压装置的挤压辊挤压压缩到一定密度后,在切断传送带上堆积成厚度均匀的米饼带,再通过切割装置切断、切割、分离等一系列动作,分割出大小适合的数等份米饼块,再经过初成型、终成型两次成型,加工出设定形状、重量的米饼,米饼最终由成型传送带输出。整个米饼的生产过程中,完全是自动的,实现了米饼的自动化生产,大大提高了生产效率,成本低,且米饼不会黏在模具上,不需要抠米饼,省时省力,降低了工作人员的负担。When making rice cakes, the cooked rice is poured into the hopper, conveyed by the hopper conveyor belt to the roller, the roller loosens the rice and distributes it evenly in the axial direction, and then sends it into the extrusion device. After being squeezed and compressed to a certain density, the rice cake belts with uniform thickness are stacked on the cutting conveyor belt, and then a series of actions such as cutting, cutting, and separation are performed by the cutting device, and several equal portions of rice cakes with suitable size are divided. Forming and final forming are carried out twice, and the rice cakes with the set shape and weight are processed, and the rice cakes are finally output by the forming conveyor belt. The entire production process of rice cakes is completely automatic, which realizes the automatic production of rice cakes, greatly improves the production efficiency, and has low cost, and the rice cakes will not stick to the mold, so there is no need to pull the rice cakes, saving time and effort, Reduce the burden on staff.
附图说明Description of drawings
图1是本实用新型米饼成型机的结构示意图;Fig. 1 is the structural representation of the rice cake forming machine of the present utility model;
图2是图1的俯视结构示意图;Fig. 2 is the top view structure schematic diagram of Fig. 1;
图3是图1中挤压装置的结构示意图;Fig. 3 is the structural representation of the extrusion device in Fig. 1;
图4是图2中饼带规整装置的结构示意图;Fig. 4 is the structural representation of the cake band regular device in Fig. 2;
图5是图1中切割装置的结构示意图;Fig. 5 is the structural representation of the cutting device in Fig. 1;
图6是图5的俯视结构示意图;Fig. 6 is the top view structure schematic diagram of Fig. 5;
图7是凸轮机构的俯视结构示意图;Fig. 7 is the top view structure schematic diagram of cam mechanism;
图8是切割装置切割米饼带时的结构示意图;Fig. 8 is the structural representation when the cutting device cuts the rice cake strip;
图9是切割装置中四把分隔刀分隔米饼块时的结构示意图;Fig. 9 is the structural representation when four dividing knives separate rice cake pieces in the cutting device;
图10是图2中推料装置旋转90°后的结构示意图;Fig. 10 is the structural schematic diagram after the pushing device in Fig. 2 is rotated by 90°;
图11是图2中分隔装置旋转90°后的结构示意图;FIG. 11 is a schematic structural diagram of the partition device in FIG. 2 after being rotated by 90°;
图12是初成型模具的结构示意图;Fig. 12 is the structural representation of the initial forming mold;
图13是本实用新型米饼成型机的工作流程图;Fig. 13 is the working flow chart of the rice cake forming machine of the present utility model;
图中:1-机架;2-料斗传送带;3-切断传送带;4-成型传送带;5-料斗;6-拨辊;7-挤压装置;70-摆臂轴;71-第一上挤压辊;72-第一下挤压辊;73-第二上挤压辊;74-第二下挤压辊;75-第三上挤压辊;76-第三下挤压辊;77-调节板;78-中间连杆;79-轴摆臂;8-饼带规整装置;81-安装架;82-导条;9-切割装置;91-滑架;92-滑架升降机构;921-滑架举升缸;922-滑架举升梁;923-滑架举升轴;924-滑架直线轴承;93-切断刀;94-连接板;95-割分机构;950-连接杆;951-分隔刀导轨;952-滑块;953-分隔刀;954-驱动杆;955-摆臂;956-摆臂轴;957-从动带轮;958-平面凸轮;9581-滑槽;959-滑架导轨;96-托架;10-推料装置;101-推料安装板;102-推料板;11-分隔装置;111-分隔安装板;112-分隔板;12-初成型模具;121-模具;122-压模;123-模具板;124-模具升降机构;1241-模具伸缩缸;1242-模具举升梁;1243-模具直线轴承;1244-模具举升轴;125-压模升降机构;1251-压模伸缩缸;1252-压模举升梁;1253-压模直线轴承;1254-压模举升轴;1255-压模连接轴;1256-螺母;1257-弹簧;13-米饼带;14-米饼块;15-初成型米饼;16-米饼;17-主动带轮。In the figure: 1-frame; 2-hopper conveyor; 3-cutting conveyor; 4-forming conveyor; 5-hopper; 6-roller; 7-extrusion device; 70-swing arm shaft; 71-first upper extrusion Press roll; 72-first lower squeeze roll; 73-second upper squeeze roll; 74-second lower squeeze roll; 75-third upper squeeze roll; 76-third lower squeeze roll; 77- Adjusting plate; 78-intermediate link; 79-axis swing arm; 8-cake belt regulation device; 81-installation frame; 82-guide bar; 9-cutting device; 91-slide frame; 92-slide frame lifting mechanism; 921 -Slide lift cylinder; 922-Slide lift beam; 923-Slide lift shaft; 924-Slide linear bearing; 93-Cut off knife; 94-Connecting plate; 95-Separation mechanism; 950-Connecting rod ;951-Separation knife guide rail;952-Slide block;953-Separation knife;954-Drive rod;955-Swing arm;956-Swing arm shaft; 959-Slide rail; 96-Bracket; 10-Pushing device; 101-Pushing installation plate; 102-Ejecting plate; 11-Separating device; 111-Separating installation plate; 112-Separating plate; Forming mold; 121-mold; 122-press mold; 123-mold plate; 124-mold lifting mechanism; 1241-mold telescopic cylinder; 1242-mold lifting beam; 1243-mold linear bearing; 1244-mold lifting shaft; 125 -Die lifting mechanism; 1251-Die telescopic cylinder; 1252-Die lifting beam; 1253-Die linear bearing; 1254-Die lifting shaft; 1255-Die connecting shaft; 1256-Nut; 1257-Spring ; 13-rice cake belt; 14-rice cake block; 15-formed rice cake; 16-rice cake; 17-active pulley.
具体实施方式Detailed ways
为了使本实用新型的目的、技术方案及优点更加清楚明白,以下结合附图及实施例,对本实用新型进行进一步详细说明。应当理解,此处所描述的具体实施例仅仅用以解释本实用新型,且不用于限定本实用新型。In order to make the purpose, technical solutions and advantages of the present utility model more clearly understood, the present utility model will be further described in detail below with reference to the accompanying drawings and embodiments. It should be understood that the specific embodiments described herein are only used to explain the present invention, and are not used to limit the present invention.
如图1和图2共同所示,一种米饼成型机,包括:机架1,沿料的运动方向,机架1上顺次设有料斗5、拨辊6、挤压装置7、饼带规整装置8、切割装置9、推料装置10、分隔装置11、初成型装置12和终成型装置13。机架1上还设有水平设置的料斗传送带2、切断传送带3和成型传送带4。As shown in Figure 1 and Figure 2 together, a rice cake forming machine includes: a
料斗5位于料斗传送带2的上方,拨辊6位于料斗传送带2下料端的上方,挤压装置7的进料口位于料斗传送带2下料端的下方,挤压装置7的出料口位于切断传送带3上料端的上方,饼带规整装置8、切割装置9和推料装置10均位于切断传送带3的上方,成型传送带4的上料端与切断传送带3的下料端相对应,切断传送带3高于成型传送带4,初成型装置12和终成型装置13位于成型传送带4的上方。The
拨辊6包括辊体,辊体上设有多个辊齿。拨辊6转动时,由辊齿将熟制的米饭打松,并让米饭沿拨辊6的轴向均匀分布。The
如图3所示,挤压装置7包括若干对沿米饭的运动方向顺次转动设置的挤压辊,每一对中的两个挤压辊间隔设置,且每一对中的两个挤压辊的间距逐渐变小。本实施例中,挤压辊设有三对,三对挤压辊分别为第一上挤压辊71和第一下挤压辊72、第二上挤压辊73和第二下挤压辊74、第三上挤压辊75和第三下挤压辊76,第二上挤压辊73和第二下挤压辊74之间间距、第三上挤压辊75和第三下挤压辊76之间间距分别通过间距调节装置调节。As shown in FIG. 3 , the
间距调节装置包括调节板77、中间连杆78和轴摆臂79,调节板77的第一端转动安装于第一上挤压辊71的端部,调节板77的第二端与中间连杆78的第一端铰接,中间连杆78的第二端与轴摆臂79的第一端铰接,轴摆臂79的第二端固定连接有摆臂轴70,摆臂轴70由电机驱动,第二上挤压辊73和第三上挤压辊75分别转动安装于调节板77上。The distance adjustment device includes an
当电机驱动摆臂轴70转动时,轴摆臂79摆动,轴摆臂79驱动中间连杆78运动,中间连杆78驱动调节板77绕第一上挤压辊71的端部转动,进而调节第二上挤压辊73与第二下挤压辊74之间间距和第三上挤压辊75与第三下挤压辊76之间间距,以根据需要挤压出不同厚度、不同密度的米饼带13。When the motor drives the
除上述结构外,也可以将第二下挤压辊74和第三下挤压辊76转动安装于调节板77,调节板77的第一端转动安装于第一下挤压辊72的端部,在此不再详细图示。In addition to the above structure, the second lower squeezing
如图4所示,饼带规整装置8包括固定设置的安装架81,安装架81固定设有两根间隔平行的导条82,导条82沿切断传送带3的长度设置。As shown in FIG. 4 , the cake
如图5、图6、图7、图8和图9共同所示,切割装置9包括沿切断传送带3宽度方向设置的滑架91,滑架91的两端分别固定有托架96,托架96连接于连接板94,每个连接板94分别连接有一套滑架升降机构92,滑架91设有切断刀93和两套分别位于滑架91两端的割分机构95,切断刀93沿切断传送带3的宽度方向设置。As shown in Figures 5, 6, 7, 8 and 9, the
滑架升降机构92包括滑架举升缸921、滑架举升梁922、滑架直线轴承924和两根滑架举升轴923,滑架举升缸921固定于机架1,滑架举升缸921与滑架举升梁922之间通过关节轴承铰接连接,两根滑架举升轴923的下端与滑架举升梁922固定,两根滑架举升轴923的上端与连接板94固定,滑架举升轴923滑动设于滑架直线轴承924内,滑架直线轴承924固定于机架1。滑架直线轴承924优选为含油轴承。The
割分机构95包括固定于滑架91且沿切断传送带宽度方向的分隔刀导轨951,分隔刀导轨951滑动连接有两个滑块952,每个滑块952均固定有一个分隔刀953,分隔刀953沿切断传送带3的长度方向延伸,每个滑块952均固定连接于驱动杆954,驱动杆954端部转动连接有滚子,滚子位于平面凸轮958的滑槽9581内,滑槽9581与切断传送带3的传送方向之间夹有锐角α,滑架91连接有用于让滑架91沿切断传送带3的长度方向往复运动的往复驱动机构。The
往复驱动机构包括滑架导轨959、摆臂955和连接杆950,滑架导轨959固定于连接板94,滑架导轨959沿切断传送带3的长度方向设置,托架96滑动于滑架导轨959,连接杆950的一端与滑架91通过关节轴承铰接,连接杆950的另一端与摆臂955的一端通过关节轴承铰接,摆臂955的另一端固定连接有摆臂轴956,摆臂轴956固定连接有从动带轮957,从动带轮957带传动连接有主动带轮17,主动带轮17由电机驱动。The reciprocating drive mechanism includes a
如图8所示,为切断刀93和分隔刀953切割米饼带13时的结构示意图,此时,两套割分机构95中分别位于最内侧的两个分隔刀953贴合在一起形成一把分隔刀。如图9所示,为分隔刀953分隔米饼块14时的结构示意图,此时,四把分隔刀953分别推动一块米饼块14沿宽度方向向外运动,将四块米饼块14分开。如图7所示,为滑架91从滑槽9581一端运动至另一端时的结构示意图。As shown in FIG. 8 , it is a schematic diagram of the structure of the cutting
如图10所示,推料装置10包括推料安装板101,推料安装板101固定于滑架91,推料安装板101固定有沿切断传送带3宽度方向均布的推料板102,推料板102推料的一侧为圆弧形,推料板102的数目与分隔刀953的数目一致。As shown in FIG. 10 , the pushing
如图11所示,切断传送带3和成型传送带4之间设有分隔装置11,分隔装置11包括沿切断传送带3宽度方向设置的分隔安装板111,分隔安装板111上固定设有沿切断传送带3宽度方向均布的分隔板112,分隔板112靠近推料板102的一端为锥形,相邻的分隔板112之间间隔形成过料通道,过料通道与推料板102的位置和数目一一对应。As shown in FIG. 11 , a
如图12所示,成型装置包括初成型模具12和终成型模具13,初成型模具12和终成型模具13的位置和数目与过料通道一一对应。初成型模具12和终成型模具13结构和工作原理相同,以初成型模具12为例,解释说明成型模具的结构和工作原理,每个初成型模具12均包括中空的模具121和在模具121内上下运动的压模122,模具121靠近分隔装置11的一侧上部开口,与圆弧形的推料板102配合形成整圆,模具121固定于模具板123,模具板123连接有模具升降机构124,压模连接有压模升降机构125。As shown in FIG. 12 , the forming device includes a preliminary forming
模具升降机构124包括模具伸缩缸1241、模具举升梁1242、模具直线轴承1243和模具举升轴1244,模具伸缩缸1241固定于机架1,模具伸缩缸1241与模具举升梁1242通过关节轴承铰接,模具举升轴1244的下端固定于模具举升梁1242,模具举升轴1244的上端与模具板123固定连接,模具举升轴1244滑动于模具直线轴承1243内,模具直线轴承1243固定于机架1。模具直线轴承1243优选为含油轴承。The
压模升降机构125包括压模伸缩缸1251、压模举升梁1252、压模直线轴承1253、压模举升轴1254和压模连接轴1255,压模伸缩缸1251固定于机架1,压模伸缩缸1251与压模举升梁1252通过关节轴承铰接,压模举升轴1254与压模举升梁1252固定,压模举升轴1254滑动于压模直线轴承1253,压模直线轴承1253固定于机架1,压模连接轴1255的下端与压模122固定连接,压模连接轴1255的上端与压模举升梁1252固定,压模连接轴1255上还固定设有螺母1256,螺母1256与压模举升梁1252之间设有套设于压模连接轴1255外的弹簧1257,每个压模122均固定连接有一根压模连接轴1255。压模直线轴承1253优选为含油轴承。The
如图13所示,本实用新型米饼成型机的工作原理和工作过程如下:As shown in Figure 13, the working principle and working process of the rice cake forming machine of the present utility model are as follows:
熟制的米饭由料斗5进入并落到料斗传送带2上,在料斗传送带2的下料端,由转动的拨辊6将米饭打松、打均后送入挤压装置7中;The cooked rice enters from the
由三对挤压辊将米饭挤压压缩成一定密度的米饼带13,米饼带13送入切断传送带3,切断传送带3上的米饼带13通过两条导条82之间的空隙时,由两条导条82对米饼带13的边缘规整,使得米饼带13的边缘整齐,米饼带13各处的宽度一致;The rice is squeezed and compressed into a certain density of
米饼带13经过切割装置9时,在初始工作位,两套割分机构95中分别位于最内侧的两个分隔刀953贴合在一起形成一把分隔刀,滑架举升缸921回缩,滑架举升轴923带动滑架91下降,使得切断刀93沿宽度方向切割下一段米饼带13,同时,三把分隔刀953共同将切割下的米饼带13沿宽度方向均分成四份米饼块14,电机通过带传动机构驱动摆臂轴956转动,摆臂轴956驱动摆臂955摆动,摆臂955通过连接杆950驱动滑架1沿滑架导轨959向切断传送带3的长度方向运动,在平面凸轮958作用下,驱动杆954向外运动,则四把分隔刀953分别驱动四块米饼块14向外运动,将四块米饼块14分开,同时,切断刀93推动四块米饼块14至四个推料板102的初始工作位,同时,四个推料板102推动上一次切割装置9切割出的四块米饼块14穿过过料通道至初成型模具12的工作位;当电机反向转动,摆臂轴956驱动摆臂955反向摆动,则滑架91反向运动复位,两套割分机构95中分别位于最内侧的两个分隔刀953贴合在一起形成一把分隔刀,同时,滑架举升缸921伸长,带动滑架91向上运动至初始位置,切断刀93、分隔刀953运动至切断传送带3上方的初始位置,四个推料板102跟随滑架91复位;When the
模具伸缩缸1241回缩,驱动模具板123向下移动,直至米饼块14位于模具121的空腔内,压模伸缩缸1251伸长,驱动压模122向下运动压缩米饼块14,米饼块14压缩成为初成型米饼15,然后模具伸缩缸1241伸长,驱动模具板123向上移动,压模伸缩缸1251回缩,驱动压模122向上运动,初成型米饼15脱离模具121支撑于成型传送带4,初成型米饼15不会黏在模具121内,成型传送带4将初成型米饼15运送至终成型模具13的工作位;The mold
终成型模具13的模具伸缩缸回缩,驱动模具板向下移动,直至初成型米饼15位于模具的空腔内,然后压模伸缩缸伸长,驱动压模向下运动压缩初成型米饼15,初成型米饼15压缩成为所需要的米饼16,然后模具伸缩缸伸长,驱动模具板向上移动,压模伸缩缸回缩,驱动压模向上运动,米饼16脱离模具支撑于成型传送带4,并由成型传送带4输送到指定位置。The mold telescopic cylinder of the final forming
本实施例中,初成型模具12和终成型模具13是相对独立的,也可以将初成型模具12和终成型模具13做成一体,即模具板上同时有初成型的模具121和终成型的模具,初成型的压模122和终成型的压模连接于同一个压模举升梁,在此不再详细图示。In this embodiment, the preliminary forming
本实施例中,一次可以生产出四个米饼16,实际工作中,可根据需要设置分隔刀953的数量,如一次切分出6块、8块等米饼块14,相应地,推料板102、过料通道、初成型的模具121和终成型的模具等也设置为6个、8个等。In this embodiment, four
本实施例中,初成型的模具121和终成型的模具为圆形,生产出的是圆形的米饼16,实际生产时,初成型的模具121和终成型的模具根据需要可以做成正方向、矩形、三角形或椭圆形等形状,在此不再一一举例。In this embodiment, the initial forming
本实用新型的米饼成型机整个米饼的生产过程中,完全是自动的,实现了米饼的自动化生产,大大提高了生产效率,成本低,且米饼不会黏在模具上,不需要抠米饼,省时省力,降低了工作人员的负担。The whole rice cake production process of the rice cake forming machine of the utility model is completely automatic, which realizes the automatic production of rice cakes, greatly improves the production efficiency, and has low cost. Picking rice cakes saves time and effort and reduces the burden on staff.
以上所述为本实用新型最佳实施方式的举例,其中未详细述及的部分均为本领域普通技术人员的公知常识。本实用新型的保护范围以权利要求的内容为准,任何基于本实用新型的技术启示而进行的等效变换,也在本实用新型的保护范围之内。The above are examples of the best embodiments of the present invention, and the parts that are not described in detail are the common knowledge of those of ordinary skill in the art. The protection scope of the present invention is subject to the content of the claims, and any equivalent transformation based on the technical inspiration of the present invention is also within the protection scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921258180.8U CN210671982U (en) | 2019-08-03 | 2019-08-03 | Rice Cake Forming Machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921258180.8U CN210671982U (en) | 2019-08-03 | 2019-08-03 | Rice Cake Forming Machine |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210671982U true CN210671982U (en) | 2020-06-05 |
Family
ID=70888924
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921258180.8U Active CN210671982U (en) | 2019-08-03 | 2019-08-03 | Rice Cake Forming Machine |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210671982U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110292146A (en) * | 2019-08-03 | 2019-10-01 | 济南好为尔机械有限公司 | Rice cake molding machine |
-
2019
- 2019-08-03 CN CN201921258180.8U patent/CN210671982U/en active Active
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110292146A (en) * | 2019-08-03 | 2019-10-01 | 济南好为尔机械有限公司 | Rice cake molding machine |
| CN110292146B (en) * | 2019-08-03 | 2024-08-13 | 好为尔机械(山东)有限公司 | Rice cake forming machine |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN207100340U (en) | A kind of biscuit fabric process equipment | |
| CN102100334B (en) | Multifunctional fry-free noodle production line and process | |
| CN107344368B (en) | A kind of jujube cake slice packaging machine | |
| CN100553460C (en) | A round steamed bun production equipment | |
| CN205040529U (en) | Multifunctional integrated filling machine | |
| CN103875749A (en) | Cat ear biscuit rolling molding unit | |
| CN106720000A (en) | Full-automatic heavy oil bread forming production line | |
| CN207040674U (en) | A kind of family's automatic dumpling making machine | |
| CN110292146B (en) | Rice cake forming machine | |
| CN2817456Y (en) | Round steamed bread producer | |
| CN203762156U (en) | Orecchiette cake rewinding and moulding machine set | |
| CN209331017U (en) | Dough extruding mechanism of egg yolk crisp production equipment | |
| CN209171287U (en) | A kind of moon cake processing quantitative segmenting device of dough | |
| CN213961545U (en) | Automatic change high-speed shaping processing equipment of filling material food | |
| CN210610897U (en) | Manual-imitation sesame candy forming slitting machine | |
| CN219920225U (en) | Sushi roll/laver roll production line | |
| CN103125543B (en) | Automatic cake rolling machine | |
| CN207461351U (en) | A kind of rice makes the special integrated machine for automatic working device people of rice flour technique | |
| CN211672182U (en) | Forming device for decorative blades in preparation of birthday peaches | |
| CN212697443U (en) | Rice product forming device | |
| CN215684512U (en) | Soft thick liquids sandwich biscuit apparatus for producing | |
| CN209660291U (en) | A moon cake forming machine | |
| CN219205714U (en) | A biscuit equipment integrating extrusion and cutting | |
| CN220987408U (en) | Red bean cake forming machine | |
| CN223772944U (en) | Round-cutting cake pressing device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address |
Address after: 251400 No.14, Shunyi street, Jibei street, Jiyang District, Jinan City, Shandong Province Patentee after: Howell machinery (Shandong) Co.,Ltd. Country or region after: China Address before: 251400 No.4 Deyang Road, Huihe Industrial Development Zone, Jiyang City, Jinan City, Shandong Province Patentee before: JINAN HIWELL MACHINERY Co.,Ltd. Country or region before: China |
|
| CP03 | Change of name, title or address |