SUMMERY OF THE UTILITY MODEL
The utility model provides a add clamping apparatus for radial drill has solved the clamping instrument commonality not good in the drilling operation, the technical problem of clamping inefficiency.
In order to achieve the above purpose, the utility model adopts the following technical scheme:
a processing clamp for a radial drilling machine comprises a base, a supporting seat, a pressing plate, a pressing seat and a locking block;
the supporting seat is embedded in the top of the base;
guide upright columns are respectively fixed on two sides of the top surface of the base and penetrate through the pressing plate;
the locking block is positioned above the pressing seat and is rotatably connected to the top of the guide upright post;
the pressing seat is arranged on the top surface of the pressing plate and is positioned right above the supporting seat.
Preferably, the side of the base is rotatably connected with an adjusting bolt, and the threaded end of the adjusting bolt is in threaded connection with the side of the supporting seat.
Preferably, waist-shaped counter bores are respectively formed in the top surfaces of the two ends of the supporting seat, and the supporting seat is fixedly connected with the base through fastening bolts located in the waist-shaped counter bores.
Preferably, the top surface of supporting seat fixedly connected with fixed support plate, fixed support plate's top surface four corners department is provided with the support column respectively.
Preferably, the top surface of the fixed supporting plate is provided with a movable supporting frame.
Preferably, the pressing seat comprises a fixed pressing plate fixed on the bottom surface of the pressing plate and a movable pressing plate movably connected on the bottom surface of the pressing plate and positioned in the fixed pressing plate.
Preferably, two ends of the top surface of the pressure plate are respectively provided with a U-shaped groove positioned below the locking block.
Preferably, the side of the locking block is provided with a horizontal handle, and the top surface of the locking block is provided with a vertical handle.
Preferably, a drill guide hole is formed in the center of the top surface of the pressure plate.
Preferably, the top of the guide upright post is sleeved with a spring positioned below the pressure plate.
In the utility model, by adopting the supporting seat with adjustable position and the locking block with adjustable locking position, the rapid clamping and fixing and the feeding and discharging of the workpiece to be drilled can be realized, the processing efficiency is ensured, and the device can be suitable for batch production; the drilling machine has the advantages that the drilling machine is suitable for drilling operation of workpieces with various sizes and different drilling positions by adopting various combinations of the fixed and detachable supporting component and the pressing component, and is good in universality and flexibility; the utility model has the advantages of simple integral structure, small volume, light weight, convenient carrying, convenient operation and use, simple and safe working process, no risk and good practicability.
Drawings
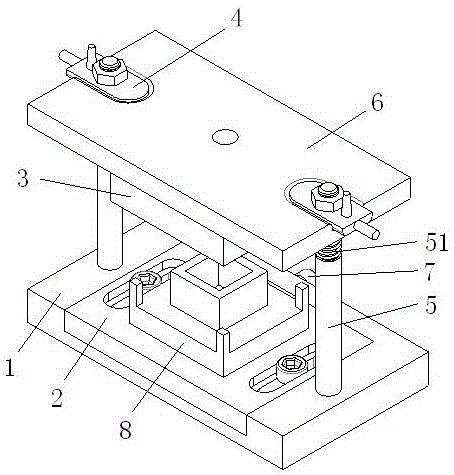
Fig. 1 is a schematic perspective view of a machining fixture for a radial drill according to the present invention;
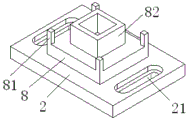
fig. 2 is a schematic perspective view of a base of a machining fixture for a radial drill according to the present invention;
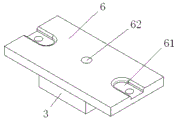
fig. 3 is one of schematic three-dimensional structural diagrams of a pressing plate of a machining fixture for a radial drilling machine according to the present invention;
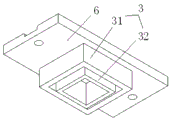
fig. 4 is a second schematic perspective view of a pressing plate of a machining fixture for a radial drill according to the present invention;
fig. 5 is the utility model provides a three-dimensional structure schematic diagram of a latch segment for radial drill's adds clamping apparatus.
Reference numbers in the figures: the device comprises a base 1, a supporting seat 2, a waist-shaped counter bore 21, a pressing block 3, a fixed pressing plate 31, a movable pressing plate 32, a locking block 4, a horizontal handle 41, a vertical handle 42, a guide upright 5, a spring 51, a pressing plate 6, a U-shaped groove 61, a drilling tool guide hole 62, an adjusting bolt 7, a fixed supporting plate 8, a supporting column 81 and a movable supporting frame 82.
Detailed Description
The technical solutions in the embodiments of the present invention will be described clearly and completely with reference to the accompanying drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only some embodiments of the present invention, not all embodiments.
Referring to fig. 1, the machining clamp for the radial drilling machine is suitable for drilling operation of parts with planar top surfaces and planar bottom surfaces and comprises a base 1, a supporting seat 2, a pressing plate 6, a pressing seat 3 and a locking block 4. Supporting seat 2 is embedded in the top of base 1, and the top surface of base 1 is provided with the caulking groove, and supporting seat 2 slides and inlays the dress in the caulking groove. The side of base 1 rotates and is connected with adjusting bolt 7, and adjusting bolt 7's screw thread end and the side threaded connection of supporting seat 2 can realize the adjustment of supporting seat 2 position on base 1 through rotating adjusting bolt 7. As shown in fig. 2, waist-shaped counter bores 21 are respectively formed in top surfaces of two ends of the support base 2, the support base 2 is fixedly connected to the base 1 through fastening bolts located in the waist-shaped counter bores 21, and the fastening bolts are used for fixing the support base 2 in the position of the base 1 after the position adjustment.
The top surface both sides of base 1 are fixed with guide upright post 5 respectively, and guide upright post 5 is at the top surface symmetric distribution of base 1, and guide upright post 5 is thick ladder cylinder structure thin from top to bottom. The top thin cylinder of the guide upright 5 penetrates the pressing plate 6, so that the pressing plate 6 can move up and down along the thin cylinder of the guide upright 5.
The locking block 4 is positioned above the pressing seat 3 and is rotatably connected to the thin column of the guide upright post 5. The top of the guide upright post 5 is provided with a thread section, and the upper part of the locking block 4 is limited by a nut which is connected to the thread section of the guide upright post 5 through a thread. As shown in fig. 3, two ends of the top surface of the pressing plate 6 are respectively provided with a U-shaped groove 61 below the locking block 4. The shape of the U-shaped groove 61 is matched with the bottom profile of the locking block 4, and when the length direction of the locking block 4 is consistent with that of the U-shaped groove 61, the locking block 4 can be embedded into the U-shaped groove 61; when the length direction of the locking block 4 is not parallel to the length direction of the U-shaped groove, two ends of the locking block 4 are lapped on the top surfaces of two sides of the U-shaped groove 61.
The top of the guide upright 5 is sleeved with a spring 51 positioned below the pressure plate 6. The spring 51 is sleeved on the thin cylinder at the top of the guide upright post 5, plays a role in buffering the moving-down process of the pressing plate 6 and plays a role in rebounding and assisting power for the moving-up of the pressing plate 6.
As shown in fig. 5, the lateral surface of the locking block 4 is provided with a horizontal handle 41, the top surface is provided with a vertical handle 42, and the horizontal handle 41/the vertical handle 42 are used for manually shifting the locking block 4 to rotate around the guide upright post 5, so as to adjust the relative position between the length direction of the locking block 4 and the length direction of the U-shaped groove 61.
As shown in fig. 2, the top surface of the supporting seat 2 is fixedly connected with a fixed supporting plate 8, and four corners of the top surface of the fixed supporting plate 8 are respectively provided with a supporting column 81. The fixed supporting plate 8 and the supporting columns 81 are used for supporting and positioning parts with large bottom surface areas. The top surface of the fixed supporting plate 8 can be provided with necessary positioning plates, positioning columns and the like according to the actual clamping and positioning requirements.
The top surface of the fixed supporting plate 8 is connected with a movable supporting frame 82 through bolts and used for supporting and positioning parts with small bottom surface areas. The movable support frame 82 is of a 'return' shape structure, the supporting surface of the movable support frame 82 is smaller than the supporting surface of the fixed supporting plate 8, and the height of the movable support frame 82 is larger than that of the supporting column 81.
The pressing seat 3 is arranged on the top surface of the pressing plate 6 and is positioned right above the supporting seat 2. As shown in fig. 4 and 5, the pressing base 3 includes a fixed pressing plate 31 fixed on the bottom surface of the pressing plate 6, and a movable pressing plate 32 bolted to the bottom surface of the pressing plate 6 and located inside the fixed pressing plate 31. The fixed pressing plate 31 and the movable pressing plate 32 are both of a structure shaped like a Chinese character 'hui', and the bottom surface of the movable pressing plate 32 protrudes out of the bottom surface of the fixed pressing plate 31. The fixed pressing plate 31 is used for pressing parts with larger top surface areas, and the movable pressing plate 32 is used for pressing parts with smaller top surface areas.
A drill guide hole 62 is provided at the center of the top surface of the pressure plate 6, and the drill guide hole 62 is located inside the movable pressure plate 32.
The utility model discloses when using, the support location and the tight fixed of clamp of work piece are realized through the combination of the 8/movable support frame 82 of fixed stay board and the 31/movable pressure strip 32 of fixed stay board, select optimum compound mode according to the size of waiting to drill work piece top surface and bottom surface area.
The specific use process of the present invention is described below with the cooperation of the fixed supporting plate 8 and the fixed pressing plate 31 as follows:
(1) adjusting and positioning:
position adjustment of the support base 2: loosening the fastening bolt, placing a workpiece to be punched on the fixed supporting plate 8, and adjusting the clamping position of the workpiece; the position of the supporting seat 2 in the caulking groove of the base 1 is adjusted through an adjusting bolt 7, so that the drilling position of the workpiece is positioned right below the drilling tool guide hole 62; and then the fastening bolt is screwed to fix the supporting seat 2 in the base 1.
Position adjustment of the locking block 4: manually applying pressure to the pressure plate 6, and rotating the locking block 4 through the horizontal handle 61 or the vertical handle 62 to ensure that the locking block 4 is vertical to the length direction of the U-shaped groove 61; and adjusting the position of a nut at the top of the guide upright post 5 on the guide upright post 5 to gradually move the pressing plate 6 downwards until the fixed pressing plate 31 is clamped on the top surface of the workpiece, wherein the pressing force reaches a preset clamping effect, and the position adjustment of the locking block 6 is completed.
The locking block 4 is reversely rotated by the horizontal handle 61 or the vertical handle 62, so that the length direction of the locking block 4 is consistent with that of the U-shaped groove 61, the pressing plate 6 moves upwards under the restoring force of the spring 51, the fixed pressing plate 31 is separated from the workpiece and is positioned above the workpiece, the workpiece is removed at the moment, and the clamp is adjusted completely and can be used for drilling.
(2) Clamping and fixing: when the workpiece is drilled, the workpiece is clamped and fixed in the same mode as the clamp adjusting process, and the drilling equipment can be started to drill the workpiece.
(3) Unlocking and blanking: after drilling is finished, the clamping force of the workpiece is relieved in the same mode as the clamp adjusting process, and the workpiece after drilling can be directly taken out from the fixed supporting plate 8.
Repeating the above process can carry out the drilling process of the next workpiece.
In the description of the present invention, it is to be understood that the terms "center", "longitudinal", "lateral", "length", "width", "thickness", "upper", "lower", "front", "rear", "left", "right", "vertical", "horizontal", "top", "bottom", "inner", "outer", "clockwise", "counterclockwise", and the like indicate orientations or positional relationships based on the orientations or positional relationships shown in the drawings, and are only for convenience of description and to simplify the description, but do not indicate or imply that the device or element referred to must have a particular orientation, be constructed and operated in a particular orientation, and therefore should not be construed as limiting the present invention.
Furthermore, the terms "first", "second" and "first" are used for descriptive purposes only and are not to be construed as indicating or implying relative importance or implicitly indicating the number of technical features indicated. Thus, a feature defined as "first" or "second" may explicitly or implicitly include one or more of that feature. In the description of the present invention, "a plurality" means two or more unless specifically limited otherwise.
The above, only be the concrete implementation of the preferred embodiment of the present invention, but the protection scope of the present invention is not limited thereto, and any person skilled in the art is in the technical scope of the present invention, according to the technical solution of the present invention and the utility model, the concept of which is equivalent to replace or change, should be covered within the protection scope of the present invention.