CN203069094U - Hinge assembly fixture in sliding door - Google Patents
Hinge assembly fixture in sliding door Download PDFInfo
- Publication number
- CN203069094U CN203069094U CN 201220717372 CN201220717372U CN203069094U CN 203069094 U CN203069094 U CN 203069094U CN 201220717372 CN201220717372 CN 201220717372 CN 201220717372 U CN201220717372 U CN 201220717372U CN 203069094 U CN203069094 U CN 203069094U
- Authority
- CN
- China
- Prior art keywords
- hinge assembly
- base
- detection
- checking tool
- slippage door
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Hinges (AREA)
Abstract
本实用新型涉及一种滑移门中铰链总成检具,其目的在于提供一种能够有效检测滑移门的中铰链总成是否合格的检具。该滑移门中铰链总成检具,包括底座,所述底座上设有用于固定铰链总成的固定块,所述底座上还设有第一检测块,该第一检测块上设有检测销,检测销的数量、位置与铰链总成上的滚轮的数量相同、位置相应。本实用新型的有益效果是:该检具操作简便,省去了人工二次对零件状态的确认步骤,加快了装配速度,提高了工作效率,适宜推广应用。
The utility model relates to a checking tool for a middle hinge assembly of a sliding door, and aims to provide a checking tool capable of effectively checking whether the middle hinge assembly of a sliding door is qualified. The hinge assembly inspection tool in the sliding door includes a base, the base is provided with a fixed block for fixing the hinge assembly, the base is also provided with a first detection block, and the first detection block is provided with a detection block. Pins, the number and position of the detection pins are the same as that of the rollers on the hinge assembly, and the positions are corresponding. The beneficial effects of the utility model are: the inspection tool is easy to operate, saves the step of manually confirming the state of the parts twice, speeds up the assembly speed, improves the work efficiency, and is suitable for popularization and application.
Description
技术领域 technical field
本实用新型涉及一种检具,尤其涉及一种用于检测滑移门的中铰链总成的检具。 The utility model relates to a checking tool, in particular to a checking tool for testing a middle hinge assembly of a sliding door.
背景技术 Background technique
车身铰链装配控制是提升车身制造水平的关键因素,滑移门装配一般是由铰链与车身进行装配后完成车身组装,车身装配前不具备对铰链来件质量检测的功能,因此不能很好的保证机盖装配的尺寸精度。对于车身铰链的精度一般用三坐标等设备进行检测,这样的操作不利于对来件质量100%的检测,且操作过程繁琐,设备投资高,不利于提高生产效率,造成生产中费工费时、效率低。 Body hinge assembly control is a key factor to improve the level of body manufacturing. Sliding door assembly is generally completed after the hinge and body are assembled. There is no function to inspect the quality of hinge incoming parts before body assembly, so it cannot be guaranteed Dimensional accuracy of cover assembly. The accuracy of the body hinges is generally tested with equipment such as three-coordinates. Such an operation is not conducive to 100% detection of the quality of the incoming parts, and the operation process is cumbersome, and the equipment investment is high, which is not conducive to improving production efficiency, resulting in time-consuming and labor-intensive production. low efficiency.
中国专利公开号CN201897451U,公开了一种轿车用铰链检测检具,包括水平测量面和检测销定位块,所述检测销定位块设置在水平测量面的一端并与水平测量面互相垂直,在所述检测销定位块上设置有安装孔,所述安装孔的数量和形状根据铰链设置的装配孔或检测孔的数量和形状设定,检测定位销插入所述安装孔内,所述检测定位销通过紧固螺钉和紧固螺母或螺纹销和螺母孔其中一种组合连接铰链并固定。该轿车用铰链检测检具无法用于检测滑移门的中铰链总成。 Chinese Patent Publication No. CN201897451U discloses a hinge inspection tool for cars, which includes a horizontal measurement surface and a detection pin positioning block. The detection pin positioning block is arranged at one end of the horizontal measurement surface and is perpendicular to the horizontal measurement surface. The detection pin positioning block is provided with mounting holes, the number and shape of the mounting holes are set according to the number and shape of the assembly holes or detection holes provided by the hinge, the detection positioning pin is inserted into the mounting hole, and the detection positioning pin The hinge is connected and fixed by a combination of fastening screws and fastening nuts or threaded pins and nut holes. The hinge inspection tool for cars cannot be used to inspect the middle hinge assembly of the sliding door.
实用新型内容 Utility model content
本实用新型的目的在于提供一种能够有效检测滑移门的中铰链总成是否合格的检具,以解决背景技术中存在的问题。 The purpose of the utility model is to provide a checking device which can effectively detect whether the middle hinge assembly of a sliding door is qualified, so as to solve the problems existing in the background technology.
为了实现上述目的,本实用新型滑移门中铰链总成检具的技术方案是:一种滑移门中铰链总成检具,包括底座,所述底座上设有用于固定铰链总成的固定块,所述底座上还设有第一检测块,该第一检测块上设有检测销,检测销的数量、位置与铰链总成上的滚轮的数量相同、位置相应。该技术方案的设计思想是:用固定块固定好铰链总成,再用检测块上的检测销对准铰链总成上的滚轮,如检测销都能准确定位,则铰链总成合格,反之不合格,该检具操作简便,省去了人工二次对零件状态的确认步骤,加快了装配速度,提高了工作效率。 In order to achieve the above object, the technical scheme of the hinge assembly inspection tool in the sliding door of the present invention is: a hinge assembly inspection tool in the sliding door, including a base, and the base is provided with a fixing bracket for fixing the hinge assembly. Block, the base is also provided with a first detection block, the first detection block is provided with detection pins, the number and position of the detection pins are the same as that of the rollers on the hinge assembly, and the positions are corresponding. The design idea of this technical solution is: fix the hinge assembly with a fixed block, and then use the detection pin on the detection block to align the rollers on the hinge assembly. If the detection pin can be positioned accurately, the hinge assembly is qualified, otherwise not. Qualified, the inspection tool is easy to operate, saves the manual second confirmation step of the part status, speeds up the assembly speed, and improves the work efficiency.
作为优选,所述固定块具有一与底座表面垂直的安装面,所述铰链总成的基准面与固定块的安装面贴合并通过夹紧器固定。夹紧器为市场上采购的标准件,其用于夹紧固定块和铰链总成从而使二者的安装面和基准面贴合。 Preferably, the fixed block has a mounting surface perpendicular to the surface of the base, and the reference plane of the hinge assembly fits with the mounting surface of the fixed block and is fixed by a clamp. The clamp is a standard part purchased in the market, which is used to clamp the fixed block and the hinge assembly so that the mounting surface and the reference surface of the two fit together.
作为优选,所述固定块的安装面上设有用于定位铰链总成的定位销。定位销用于铰链总成安装到固定块上时起到定位找准的作用。 Preferably, a positioning pin for positioning the hinge assembly is provided on the mounting surface of the fixing block. The positioning pin is used for positioning and alignment when the hinge assembly is installed on the fixed block.
作为优选,所述底座上还设有第二检测块,该第二检测块具有与底座表面垂直的检测面,该检测面与铰链总成的滚轮安装孔所在面的间隙可通过插入预设厚度的间隙塞尺而检测间隙误差。铰链总成的基准面固定到固定块上后,铰链总成的活动端仍可转动,其转到靠近第二检测块的检测面的极限位置时,活动端面与检测面之间存有间隙,之后插入预设厚度的间隙塞尺,记录下间隙可判断其误差。 Preferably, the base is also provided with a second detection block, the second detection block has a detection surface perpendicular to the surface of the base, the gap between the detection surface and the surface where the roller mounting hole of the hinge assembly is located can be inserted into a preset thickness The clearance feeler gauge is used to detect the clearance error. After the reference surface of the hinge assembly is fixed on the fixed block, the movable end of the hinge assembly can still rotate, and when it turns to the extreme position close to the detection surface of the second detection block, there is a gap between the movable end surface and the detection surface. Then insert a gap feeler gauge with a preset thickness, and record the gap to judge its error.
作为优选,所述第一检测块包括垂直于底座的竖板,竖板顶部设有与其垂直的横板。 Preferably, the first detection block includes a vertical plate perpendicular to the base, and a horizontal plate perpendicular to the vertical plate is provided on the top of the vertical plate.
作为优选,所述竖板上设有垂直其表面的一个检测销。 Preferably, a detection pin perpendicular to the surface of the riser is provided.
作为优选,所述横板上设有垂直其表面的二个检测销。以上竖板和横板上检测销的位置都是根据铰链总成上滚轮位置而设定。 Preferably, the horizontal plate is provided with two detection pins perpendicular to its surface. The positions of the detection pins on the above vertical plate and the horizontal plate are all set according to the position of the rollers on the hinge assembly.
作为优选,所述检测销的面向铰链总成上的滚轮的端面上设有可容纳滚轮并与之适配的定位孔。 Preferably, the end surface of the detection pin facing the roller on the hinge assembly is provided with a positioning hole that can accommodate the roller and fit therewith.
本实用新型滑移门中铰链总成检具的有益效果是:该检具操作简便,省去了人工二次对零件状态的确认步骤,加快了装配速度,提高了工作效率。 The beneficial effect of the hinge assembly inspection tool in the sliding door of the utility model is that the inspection tool is easy to operate, saves the manual secondary confirmation step of the parts state, speeds up the assembly speed, and improves the work efficiency.
附图说明 Description of drawings
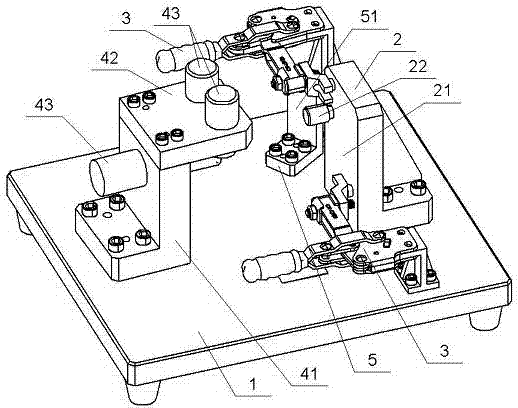
图1为本实用新型滑移门中铰链总成检具的一种结构示意图; Fig. 1 is a structural schematic diagram of the hinge assembly checker in the sliding door of the present invention;
图2为图1的后方视角示意图; FIG. 2 is a schematic view of the rear view of FIG. 1;
图3为本实用新型滑移门中铰链总成检具的俯视图; Fig. 3 is a top view of the hinge assembly inspection tool in the sliding door of the present invention;
图4为本实用新型滑移门中铰链总成检具的使用状态示意图。 Fig. 4 is a schematic diagram of the use state of the hinge assembly inspection tool in the sliding door of the present invention.
图中标号分别为:1.底座 2.固定块 21.安装面 22.定位销 3.夹紧器 41.竖板 42.横板 43.检测销 5.第二检测块 51.检测面 6.铰链总成。
The labels in the figure are: 1.
具体实施方式 Detailed ways
下面通过实施例并结合附图对本实用新型的技术方案作进一步的具体描述。 The technical solution of the utility model will be further specifically described below through the embodiments and in conjunction with the accompanying drawings.
实施例: Example:
一种滑移门中铰链总成检具,如图1至图3所示,包括底座1,所述底座1上设有用于固定铰链总成6的固定块2,所述固定块2具有一与底座1表面垂直的安装面21,所述铰链总成6的基准面与固定块2的安装面21贴合并通过夹紧器3固定,所述固定块2的安装面21上设有用于定位铰链的定位销22,所述底座1上还设有第一检测块,所述第一检测块包括垂直于底座1的竖板41,竖板41顶部设有与其垂直的横板42,所述竖板41上设有垂直其表面的一个检测销43,所述横板42上设有垂直其表面的二个检测销43,该检测销43与铰链总成6上的滚轮位置相应,所述检测销43的面向铰链上的滚轮的端面上设有可容纳滚轮并与之适配的定位孔,所述底座1上还设有第二检测块5,该第二检测块5具有与底座1表面垂直的检测面51,该检测面51与铰链总成6的滚轮安装孔所在面的间隙可通过插入预设厚度的间隙塞尺而检测间隙误差。
A hinge assembly inspection tool in a sliding door, as shown in Figures 1 to 3, includes a
使用时,如图4所示,用夹紧器3把铰链总成6固定到固定块2上使铰链总成6的基准面和固定块2的安装面21贴合,转动铰链总成6的活动端使其上的滚轮与第一检测块上的检测销43对应,如滚轮都能准确进入检测销上的定位孔内,则铰链总成6合格,反之不合格。
When in use, as shown in Figure 4, the
上述所描述的具体实施例仅仅是对本实用新型的构思作优选举例说明。凡在本实用新型的精神和原则之内所做的任何修改或补充或等同替代,均应包含在本实用新型权利要求的保护范围之内。 The specific embodiments described above are only preferred illustrations for the concept of the present utility model. Any modification, supplement or equivalent replacement made within the spirit and principle of the present utility model shall be included in the protection scope of the claims of the utility model.
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201220717372 CN203069094U (en) | 2012-12-24 | 2012-12-24 | Hinge assembly fixture in sliding door |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201220717372 CN203069094U (en) | 2012-12-24 | 2012-12-24 | Hinge assembly fixture in sliding door |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203069094U true CN203069094U (en) | 2013-07-17 |
Family
ID=48767872
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201220717372 Expired - Fee Related CN203069094U (en) | 2012-12-24 | 2012-12-24 | Hinge assembly fixture in sliding door |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203069094U (en) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103954189A (en) * | 2014-05-08 | 2014-07-30 | 安徽大昌科技股份有限公司 | Automobile instrument board beam left support assembly detection tool |
| CN103954188A (en) * | 2014-05-08 | 2014-07-30 | 安徽大昌科技股份有限公司 | Automobile instrument board beam assembly detection tool |
| CN104501675A (en) * | 2014-11-24 | 2015-04-08 | 上海奥林汽车安全系统有限公司 | Four-connection rod front cover hinge assembly detection tool |
| CN104501677A (en) * | 2014-11-24 | 2015-04-08 | 上海奥林汽车安全系统有限公司 | Front cover hinge assembly detection tool |
| CN104501678A (en) * | 2014-11-24 | 2015-04-08 | 上海奥林汽车安全系统有限公司 | Auto front door hinge assembly detection tool |
| CN105202993A (en) * | 2015-09-29 | 2015-12-30 | 上海奥林汽车安全系统有限公司 | Testing tool for automobile front-cover hinge assembly |
-
2012
- 2012-12-24 CN CN 201220717372 patent/CN203069094U/en not_active Expired - Fee Related
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103954189A (en) * | 2014-05-08 | 2014-07-30 | 安徽大昌科技股份有限公司 | Automobile instrument board beam left support assembly detection tool |
| CN103954188A (en) * | 2014-05-08 | 2014-07-30 | 安徽大昌科技股份有限公司 | Automobile instrument board beam assembly detection tool |
| CN104501675A (en) * | 2014-11-24 | 2015-04-08 | 上海奥林汽车安全系统有限公司 | Four-connection rod front cover hinge assembly detection tool |
| CN104501677A (en) * | 2014-11-24 | 2015-04-08 | 上海奥林汽车安全系统有限公司 | Front cover hinge assembly detection tool |
| CN104501678A (en) * | 2014-11-24 | 2015-04-08 | 上海奥林汽车安全系统有限公司 | Auto front door hinge assembly detection tool |
| CN104501677B (en) * | 2014-11-24 | 2017-02-22 | 上海奥林汽车安全系统有限公司 | Front cover hinge assembly detection tool |
| CN104501678B (en) * | 2014-11-24 | 2017-02-22 | 上海奥林汽车安全系统有限公司 | Auto front door hinge assembly detection tool |
| CN104501675B (en) * | 2014-11-24 | 2020-03-31 | 上海奥林汽车安全系统有限公司 | Four-bar linkage front cover hinge assembly checking fixture |
| CN105202993A (en) * | 2015-09-29 | 2015-12-30 | 上海奥林汽车安全系统有限公司 | Testing tool for automobile front-cover hinge assembly |
| CN105202993B (en) * | 2015-09-29 | 2020-03-31 | 上海奥林汽车安全系统有限公司 | Detection tool for automobile front cover hinge assembly |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102853730B (en) | Automobile engine hood hinge inspection tool | |
| CN204988102U (en) | Blade comprehensive testing device | |
| CN106403752A (en) | Automobile stamping part size and position accuracy rapid detection assembly | |
| CN205066613U (en) | Hinge detection device | |
| CN106525352B (en) | A device for detecting the tightness of welded parts | |
| CN105698637A (en) | Test tool for engine mounting bracket | |
| CN204438953U (en) | A kind of fore sub frame assembly measures support | |
| CN202692882U (en) | Engine exhaust pipe inspection device | |
| CN202599317U (en) | Static contact component assembling inspection tool of circuit breaker | |
| CN203069097U (en) | Hinge and roller detecting tool for automobile slide door | |
| CN108645307A (en) | A kind of member fitted position measurement tooling | |
| CN205748236U (en) | Spinning frame roller is every the calibration equipment of tool set pattern detection faces perpendicularity | |
| CN204154296U (en) | A kind of structure of comprehensive check tool of turbine case | |
| CN104048575A (en) | Measurement device for automobile front-cover inner-plate hinge reinforcement plate | |
| CN204666060U (en) | A kind of variator bonnet comprehensively tests tool | |
| CN204705286U (en) | Novel cable pulley type glass lifter guide rail cubing | |
| CN202928486U (en) | Detection device used to detect irregular structure geometric tolerance | |
| CN204240888U (en) | Automobile gliding groove upper cover plate pick-up unit | |
| CN207147375U (en) | The parallel set pattern composition error calibration equipment of fly frame front roller of weaving | |
| CN216299051U (en) | A special tool for the inspection of the accuracy of the angle between the spline and the swing arm on the spline shaft | |
| CN205957844U (en) | Bridge plate for measuring position precision between prismatic guide rail and dovetail guide rail | |
| CN204974814U (en) | Detection instrument of punching press part size | |
| CN217900701U (en) | Lithium battery thickness measuring device | |
| CN218600443U (en) | Battery case R angle department thickness detection device | |
| CN205825843U (en) | A kind of guide block comprehensive check tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20130717 Termination date: 20141224 |
|
| EXPY | Termination of patent right or utility model |