CN116252539A - Fluorocarbon paint overprinting technology positioner - Google Patents
Fluorocarbon paint overprinting technology positioner Download PDFInfo
- Publication number
- CN116252539A CN116252539A CN202211538982.0A CN202211538982A CN116252539A CN 116252539 A CN116252539 A CN 116252539A CN 202211538982 A CN202211538982 A CN 202211538982A CN 116252539 A CN116252539 A CN 116252539A
- Authority
- CN
- China
- Prior art keywords
- overprinting
- positioning
- frame
- rack
- fluorocarbon paint
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images


Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65G—TRANSPORT OR STORAGE DEVICES, e.g. CONVEYORS FOR LOADING OR TIPPING, SHOP CONVEYOR SYSTEMS OR PNEUMATIC TUBE CONVEYORS
- B65G23/00—Driving gear for endless conveyors; Belt- or chain-tensioning arrangements
- B65G23/24—Gearing between driving motor and belt- or chain-engaging elements
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F17/00—Printing apparatus or machines of special types or for particular purposes, not otherwise provided for
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41F—PRINTING MACHINES OR PRESSES
- B41F23/00—Devices for treating the surfaces of sheets, webs, or other articles in connection with printing
- B41F23/04—Devices for treating the surfaces of sheets, webs, or other articles in connection with printing by heat drying, by cooling, by applying powders
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65G—TRANSPORT OR STORAGE DEVICES, e.g. CONVEYORS FOR LOADING OR TIPPING, SHOP CONVEYOR SYSTEMS OR PNEUMATIC TUBE CONVEYORS
- B65G47/00—Article or material-handling devices associated with conveyors; Methods employing such devices
- B65G47/74—Feeding, transfer, or discharging devices of particular kinds or types
- B65G47/82—Rotary or reciprocating members for direct action on articles or materials, e.g. pushers, rakes, shovels
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41P—INDEXING SCHEME RELATING TO PRINTING, LINING MACHINES, TYPEWRITERS, AND TO STAMPS
- B41P2217/00—Printing machines of special types or for particular purposes
- B41P2217/10—Printing machines of special types or for particular purposes characterised by their constructional features
- B41P2217/12—Machines with reversible printing units
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41P—INDEXING SCHEME RELATING TO PRINTING, LINING MACHINES, TYPEWRITERS, AND TO STAMPS
- B41P2217/00—Printing machines of special types or for particular purposes
- B41P2217/50—Printing presses for particular purposes
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B41—PRINTING; LINING MACHINES; TYPEWRITERS; STAMPS
- B41P—INDEXING SCHEME RELATING TO PRINTING, LINING MACHINES, TYPEWRITERS, AND TO STAMPS
- B41P2251/00—Details or accessories of printing machines not otherwise provided for
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Coating Apparatus (AREA)
Abstract
本发明公开了一种氟碳漆套印工艺定位装置,属于套印设备技术领域,包括防护壳、套印机构、输送机构、定位机构、下料机构、烘干机构;所述的套印机构包括套印模具,所述的套印模具用于对加工件进行套印,所述的套印模具安装在升降组件上;所述的定位机构包括水平架,所述的水平架上设置两个对称布置的定位组件,所述的定位组件用于对加工件进行定位。本发明通过套印机构、输送机构、定位机构、下料机构和烘干机构自动完成对工件的套印和烘干,结构简单,操作方便。
The invention discloses a positioning device for fluorocarbon paint overprinting process, which belongs to the technical field of overprinting equipment and includes a protective shell, an overprinting mechanism, a conveying mechanism, a positioning mechanism, a blanking mechanism, and a drying mechanism; the overprinting mechanism includes an overprinting mold, The overprinting mold is used to overprint the workpiece, and the overprinting mold is installed on the lifting assembly; the positioning mechanism includes a horizontal frame, and two symmetrically arranged positioning components are arranged on the horizontal frame. The positioning component is used to position the workpiece. The invention automatically completes the overprinting and drying of the workpiece through the overprinting mechanism, the conveying mechanism, the positioning mechanism, the feeding mechanism and the drying mechanism, and has simple structure and convenient operation.
Description
技术领域technical field
本发明属于套印设备技术领域,特别涉及一种氟碳漆套印工艺定位装置。The invention belongs to the technical field of overprinting equipment, in particular to a positioning device for fluorocarbon paint overprinting process.
背景技术Background technique
在对工件进行氟碳漆套印处理时,需要对被套印的工件进行固定,防止工件位置偏差,导致套印不准确。所以在对工件进行套印的时候,需要对工件进行精确的定位,保证套印的质量。When the fluorocarbon paint is overprinted on the workpiece, it is necessary to fix the overprinted workpiece to prevent the position deviation of the workpiece and cause inaccurate overprinting. Therefore, when overprinting the workpiece, it is necessary to accurately position the workpiece to ensure the quality of overprinting.
公告号为CN215397584U的发明专利公开了一种并联式套印生产系统,所述并联式套印生产系统包括第一传送机构、丝印机构组和第二传送机构,所述第一传送机构用于接收板料,并将待丝印板料传递至丝印机构,所述第二传送机构用于将在丝印机构处完成丝印工艺的板料传递至后处理工艺端。公开号为CN110920285A的中国发明专利公开了一种用于转移纸二次定位套印工艺,提供一种制作由多个不同防伪文字和外形的图案、且各图案间位置尺寸精密保证的多个图案按设计要求用油墨图案与全息图案进行定位印刷在纸上、使包装纸整个表面带有防伪文字和图案的二次定位全息防伪印刷方法及其二次定位全息防伪印刷纸。尽管该发明能够完成套印,但是不能对加工件进行定位,并且不便于进行上下料。针对以上问题,本发明提供了一种氟碳漆套印工艺定位装置。The invention patent with the notification number CN215397584U discloses a parallel overprint production system. The parallel overprint production system includes a first transmission mechanism, a silk screen mechanism group and a second transmission mechanism. The first transmission mechanism is used to receive sheet materials , and transfer the sheet to be screen-printed to the screen-printing mechanism, and the second transfer mechanism is used to transfer the sheet that has been screen-printed at the screen-printing mechanism to the end of the post-processing process. The Chinese invention patent with the publication number CN110920285A discloses a process for secondary positioning and overprinting of transfer paper, which provides a method for making multiple patterns with different anti-counterfeiting characters and shapes, and the position and size of each pattern are precisely guaranteed. The design requires printing ink pattern and holographic pattern on the paper, so that the entire surface of the wrapping paper has anti-counterfeiting characters and patterns. The secondary positioning holographic anti-counterfeiting printing method and the secondary positioning holographic anti-counterfeiting printing paper. Although the invention can complete overprinting, it cannot position the workpiece and is inconvenient for loading and unloading. In view of the above problems, the present invention provides a positioning device for fluorocarbon paint overprinting process.
发明内容Contents of the invention
针对上述技术问题,本发明所采用的技术方案是:一种氟碳漆套印工艺定位装置,包括防护壳;还包括安装在防护壳内部的套印机构、输送机构、定位机构、下料机构、烘干机构。In view of the above technical problems, the technical solution adopted in the present invention is: a fluorocarbon paint overprint process positioning device, including a protective shell; Dry institutions.
所述的套印机构包括套印模具,所述的套印模具用于对加工件进行套印,所述的套印模具安装在升降组件上。The overprinting mechanism includes an overprinting mold, which is used for overprinting the workpiece, and the overprinting mold is installed on the lifting assembly.
所述的定位机构包括水平架,所述的水平架上设置两个对称布置的定位组件,所述的定位组件用于对加工件进行定位。The positioning mechanism includes a horizontal frame, and two symmetrically arranged positioning components are arranged on the horizontal frame, and the positioning components are used for positioning the workpiece.
进一步的,所述的升降组件包括双向齿条,所述的双向齿条与套印模具固定连接,双向齿条滑动安装在竖直导向杆上,所述的竖直导向杆固定安装在防护壳内部的上端,竖直导向杆的外圈套设有复位弹簧一,所述的复位弹簧一一端固定在双向齿条上,复位弹簧一的另一端固定在竖直导向杆上,双向齿条的一侧与不完全齿轮啮合配合,所述的不完全齿轮转动安装在安装架上,所述的安装架固定安装在防护壳的内部,不完全齿轮与电机的输出轴固定连接,电机安装在防护壳的内部。Further, the lifting assembly includes a two-way rack, the two-way rack is fixedly connected to the overprinting mold, the two-way rack is slidably installed on a vertical guide rod, and the vertical guide rod is fixedly installed inside the protective shell The upper end of the vertical guide bar is provided with a return spring one, and one end of the return spring one is fixed on the two-way rack, and the other end of the return spring one is fixed on the vertical guide bar, and one end of the two-way rack is fixed on the vertical guide bar. The side meshes with the incomplete gear, the incomplete gear is rotated and installed on the mounting frame, the mounting frame is fixedly installed inside the protective shell, the incomplete gear is fixedly connected with the output shaft of the motor, and the motor is installed in the protective shell internal.
进一步的,所述的套印机构还包括圆柱齿轮,所述的圆柱齿轮与不完全齿轮分别位于双向齿条的两侧,所述的圆柱齿轮安装在传动轴外圈,且圆柱齿轮的内圈设置的限位棘轮与传动轴上设置的棘爪形成棘轮棘爪配合,所述的传动轴转动安装在安装架上。Further, the overprint mechanism also includes a cylindrical gear, the cylindrical gear and the incomplete gear are respectively located on both sides of the bidirectional rack, the cylindrical gear is installed on the outer ring of the transmission shaft, and the inner ring of the cylindrical gear is set The limit ratchet and the pawl arranged on the transmission shaft form a ratchet pawl cooperation, and the transmission shaft is rotatably mounted on the mounting frame.
进一步的,所述的双向齿条下方滑动安装有驱动架,所述的驱动架位于套印模具与双向齿条之间,且所述的驱动架与双向齿条之间设置有复位弹簧二。Further, a driving frame is slidably installed under the bidirectional rack, and the driving frame is located between the overprinting mold and the bidirectional rack, and a return spring 2 is arranged between the driving frame and the bidirectional rack.
进一步的,所述的输送机构包括皮带组件,所述的皮带组件一端与传动轴连接,形成带轮配合,皮带组件的另一端与水平轴连接,形成带轮配合,所述的水平轴另一端与圆锥齿轮组的输入端连接,所述的圆锥齿轮组的输出端与传送带的一端连接,所述的传送带安装在防护壳的内部底端。Further, the conveying mechanism includes a belt assembly, one end of the belt assembly is connected to the transmission shaft to form a pulley fit, the other end of the belt assembly is connected to a horizontal shaft to form a pulley fit, and the other end of the horizontal shaft It is connected with the input end of the bevel gear set, and the output end of the bevel gear set is connected with one end of the conveyor belt, and the conveyor belt is installed at the inner bottom of the protective shell.
进一步的,所述的定位组件包括定位板,所述的定位板上固定安装有两个连接杆的一端,所述的连接杆的另一端与挤压板固定连接,所述的连接杆滑动安装在水平架上,且所述的挤压板与水平架之间设置有复位弹簧三。Further, the positioning assembly includes a positioning plate, one end of two connecting rods is fixedly installed on the positioning plate, the other end of the connecting rod is fixedly connected with the extrusion plate, and the connecting rod is slidably installed On the horizontal frame, a return spring three is arranged between the extruding plate and the horizontal frame.
进一步的,所述的下料机构包括推杆、球头杆,所述的推杆与一个挤压板固定连接,球头杆的一端转动安装有球,所述的球与推杆滑动配合,所述的球头杆的另一端与三脚架固定连接,球头杆滑动安装在导向架上,所述的导向架固定安装在水平架上,所述的三脚架上远离推杆的一侧为斜面,三脚架与储料筒下方的槽滑动配合,所述的储料筒内部放置有多个待加工的加工件,所述的储料筒设置在防护壳的内部。Further, the blanking mechanism includes a push rod and a ball head rod, the push rod is fixedly connected with an extruded plate, a ball is installed on one end of the ball head rod, and the ball is slidably matched with the push rod, The other end of the ball stud is fixedly connected to the tripod, the ball stud is slidably mounted on the guide frame, the guide frame is fixedly mounted on the horizontal frame, and the side of the tripod far away from the push rod is an inclined plane, The tripod is slidably matched with the groove below the material storage tube. A plurality of workpieces to be processed are placed inside the material storage tube, and the material storage tube is arranged inside the protective shell.
进一步的,所述的烘干机构包括外箱,所述的外箱固定安装在防护壳的内部,且电机位于外箱的内部,外箱上连接有导热管的一端,所述的导热管的另一端滑动安装有压合头,压合头与导热管之间设置有复位弹簧五,压合头的上方固定安装有滑动板的一端,滑动板的另一端设置在驱动架下方,所述的滑动板与U形导向杆滑动配合,所述的U形导向杆固定安装在防护壳的内部底端。Further, the drying mechanism includes an outer box, the outer box is fixedly installed inside the protective shell, and the motor is located inside the outer box, one end of the heat pipe is connected to the outer box, and the heat pipe The other end is slidably installed with a pressing head, and a
本发明与现有技术相比的有益效果是:(1)本发明通过套印机构、输送机构、定位机构、下料机构和烘干机构自动完成对工件的套印和烘干,结构简单,操作方便;(2)套印机构、输送机构、定位机构、下料机构和烘干机构通过电机一个动力源完成驱动,节约动力,并且电机产生的热量还可以通过烘机构对套印完的加工件进行烘干,实现了对能源的利用;(3)在定位机构对加工件进行定位的同时,下料机构中的三脚架将储料筒中的加工件送出,节约了输送的时间。The beneficial effects of the present invention compared with the prior art are: (1) The present invention automatically completes the overprinting and drying of the workpiece through the overprinting mechanism, the conveying mechanism, the positioning mechanism, the blanking mechanism and the drying mechanism, with simple structure and convenient operation ; (2) The overprinting mechanism, conveying mechanism, positioning mechanism, feeding mechanism and drying mechanism are driven by one power source of the motor to save power, and the heat generated by the motor can also be used to dry the overprinted workpiece through the drying mechanism , to realize the utilization of energy; (3) While the positioning mechanism is positioning the workpiece, the tripod in the unloading mechanism sends the workpiece out of the storage tank, saving the transportation time.
附图说明Description of drawings
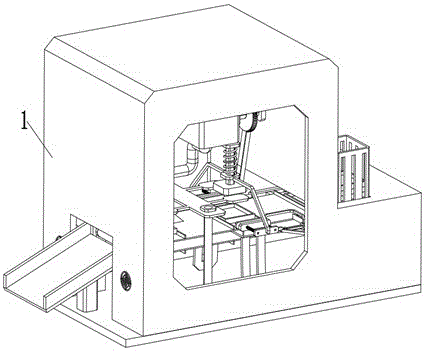
图1为本发明整体结构示意图。Figure 1 is a schematic diagram of the overall structure of the present invention.
图2为烘干机构结构示意图。Figure 2 is a schematic diagram of the structure of the drying mechanism.
图3为图1省略防护壳以外其余结构示意图。Fig. 3 is a schematic diagram of the rest of the structure in Fig. 1 omitting the protective case.
图4为图3另一角度结构示意图。FIG. 4 is a schematic structural diagram of another angle of FIG. 3 .
图5为图4中A处局部放大结构示意图。FIG. 5 is a schematic diagram of a partially enlarged structure at A in FIG. 4 .
图6为套印机构结构示意图。Fig. 6 is a structural schematic diagram of the overprinting mechanism.
图7为套印机构部分结构示意图。Fig. 7 is a schematic diagram of the partial structure of the overprinting mechanism.
图8为定位机构结构示意图。Fig. 8 is a structural schematic diagram of the positioning mechanism.
图9为下料机构结构示意图。Fig. 9 is a structural schematic diagram of the unloading mechanism.
图10为图9中B处局部放大结构示意图。FIG. 10 is a schematic diagram of a partially enlarged structure at B in FIG. 9 .
附图标号:1-防护壳;2-套印机构;201-电机;202-不完全齿轮;203-安装架;204-双向齿条;205-竖直导向杆;206-复位弹簧一;207-圆柱齿轮;208-限位棘轮;209-传动轴;210-套印模具;211-复位弹簧二;212-驱动架;3-输送机构;301-皮带组件;302-水平轴;303-圆锥齿轮组;304-传送带;4-定位机构;401-水平架;402-定位板;403-连接杆;404-挤压板;405-复位弹簧三;5-下料机构;501-推杆;502-球头杆;503-复位弹簧四;504-三脚架;505-储料筒;506-导向架;6-烘干机构;601-外箱;602-导热管;603-压合头;604-复位弹簧五;605-滑动板;606-U形导向杆;7-夹持架;8-加工件。Reference numerals: 1-protective shell; 2-overprint mechanism; 201-motor; 202-incomplete gear; 203-installation frame; 204-two-way rack; 205-vertical guide rod; Cylindrical gear; 208-limiting ratchet; 209-transmission shaft; 210-overprinting mold; 211-return spring two; 212-drive frame; ; 304-conveyor belt; 4-positioning mechanism; 401-level frame; 402-positioning plate; Ball head rod; 503-return spring four; 504-tripod; 505-storage barrel; 506-guide frame; 6-drying mechanism; 601-outer box; Spring five; 605-sliding plate; 606-U-shaped guide rod; 7-clamping frame; 8-workpiece.
具体实施方式Detailed ways
下面结合附图并通过具体实施方式来进一步说明本发明的技术方案。The technical solutions of the present invention will be further described below in conjunction with the accompanying drawings and through specific implementation methods.
其中,附图仅用于示例性说明,表示的仅是示意图,而非实物图,不能理解为对本专利的限制,为了更好地说明本发明的实施例,附图某些部件会有省略、放大或缩小,并不代表实际产品的尺寸,对本领域技术人员来说,附图中某些公知结构及其说明可能省略是可以理解的。Wherein, the accompanying drawings are only for illustrative purposes, showing only schematic diagrams, rather than actual pictures, and should not be understood as limitations on this patent. In order to better illustrate the embodiments of the present invention, some parts of the accompanying drawings will be omitted Enlargement or reduction does not represent the size of the actual product. For those skilled in the art, it is understandable that certain known structures and their descriptions may be omitted in the drawings.
实施例:如图1—图10所示的一种氟碳漆套印工艺定位装置,包括防护壳1,还包括安装在防护壳1内部的套印机构2、输送机构3、定位机构4、下料机构5、烘干机构6。Embodiment: a positioning device for fluorocarbon paint overprinting process as shown in Fig. 1-Fig.
套印机构2包括套印模具210,套印模具210用于对加工件8进行套印,套印模具210安装在升降组件上。The overprinting mechanism 2 includes an
定位机构4包括水平架401,水平架401上设置两个对称布置的定位组件,定位组件用于对加工件8进行定位。The
升降组件包括双向齿条204,双向齿条204与套印模具210固定连接,双向齿条204滑动安装在竖直导向杆205上,竖直导向杆205固定安装在防护壳1内部的上端,竖直导向杆205的外圈套设有复位弹簧一206,复位弹簧一206一端固定在双向齿条204上,复位弹簧一206的另一端固定在竖直导向杆205上,双向齿条204的一侧与不完全齿轮202啮合配合,不完全齿轮202转动安装在安装架203上,安装架203固定安装在防护壳1的内部,不完全齿轮202与电机201的输出轴固定连接,电机201安装在防护壳1的内部。The lifting assembly includes a two-
套印机构2还包括圆柱齿轮207,圆柱齿轮207与不完全齿轮202分别位于双向齿条204的两侧,圆柱齿轮207安装在传动轴209外圈,且圆柱齿轮207的内圈设置的限位棘轮208与传动轴209上设置的棘爪形成棘轮棘爪配合,传动轴209转动安装在安装架203上。The overprint mechanism 2 also includes a
双向齿条204下方滑动安装有驱动架212,驱动架212位于套印模具210与双向齿条204之间,且驱动架212与双向齿条204之间设置有复位弹簧二211。A
输送机构3包括皮带组件301,皮带组件301一端与传动轴209连接,形成带轮配合,皮带组件301的另一端与水平轴302连接,形成带轮配合,水平轴302另一端与圆锥齿轮组303的输入端连接,圆锥齿轮组303的输出端与传送带304的一端连接,传送带304安装在防护壳1的内部底端。The
定位组件包括定位板402,定位板402上固定安装有两个连接杆403的一端,连接杆403的另一端与挤压板404固定连接,连接杆403滑动安装在水平架401上,且挤压板404与水平架401之间设置有复位弹簧三405。The positioning assembly includes a
下料机构5包括推杆501、球头杆502,推杆501与一个挤压板404固定连接,球头杆502的一端转动安装有球,球与推杆501滑动配合,球头杆502的另一端与三脚架504固定连接,球头杆502滑动安装在导向架506上,导向架506固定安装在水平架401上,三脚架504上远离推杆501的一侧为斜面,三脚架504与储料筒505下方的槽滑动配合,储料筒505内部放置有多个待加工的加工件8,储料筒505设置在防护壳1的内部。
烘干机构6包括外箱601,外箱601固定安装在防护壳1的内部,且电机201位于外箱601的内部,外箱601上连接有导热管602的一端,导热管602的另一端滑动安装有压合头603,压合头603与导热管602之间设置有复位弹簧五604,压合头603的上方固定安装有滑动板605的一端,滑动板605的另一端设置在驱动架212下方,滑动板605与U形导向杆606滑动配合,U形导向杆606固定安装在防护壳1的内部底端。The
工作原理:启动电机201,使电机201的输出轴带动不完全齿轮202转动,当不完全齿轮202上有齿的部分转动到与双向齿条204啮合的时候,双向齿条204会在不完全齿轮202的驱动下沿着竖直导向杆205向下滑动,这个过程中会压缩位于双向齿条204与竖直导向杆205之间的复位弹簧一206,复位弹簧一206的作用是辅助双向齿条204的复位。双向齿条204向下移动的过程中,安装在双向齿条204下方的套印模具210就会移动,且滑动安装在双向齿条204下方的驱动架212会一起向下移动。Working principle: Start the
由于驱动架212的两端为斜面,所以驱动架212在向下移动的过程中,会将位于水平架401两侧的挤压板404向相互靠近的方向移动,挤压板404通过连接杆403与定位板402连接,所以两个定位板402会逐渐靠近,此时通过传送带304输送过来的加工件8就会被两个定位板402夹紧,完成固定定位。需要说明的是,传送带304上设置有多个夹持架7,夹持架7用于装载加工件8,并且定位板402的宽度保证了定位板402能够在夹持架7的内部滑动。Since the two ends of the
向下移动的套印模具210触碰到通过定位板402定位的加工件8,在套印模具210向下移动的时候,就完成了对加工件8的套印。需要说明的是,由于驱动架212滑动安装在双向齿条204上,所以在驱动架212推动挤压板404到最大限度的时候,驱动架212被挤压板404卡住,这时候双向齿条204和套印模具210向下移动的过程中,复位弹簧二211会被压缩,即使驱动架212不再向下移动,也不会限制套印模具210的运动,同时复位弹簧二211还有助于辅助驱动架212的复位。The
此外,由于圆柱齿轮207上的限位棘轮208与传动轴209上的棘爪形成了棘轮棘爪配合,所以在双向齿条204向下的过程中即使圆柱齿轮207会转动,也不会使传动轴209转动,这样皮带组件301就不会转动,那么传送带304就不会转动,这样做的目的在于使传送带304保持静止,为套印模具210对加工件8进行套印提供静止环境。In addition, because the
在电机201带动不完全齿轮202转动到没有齿的部分朝向双向齿条204的时候,此时不完全齿轮202不再与双向齿条204啮合,那么双向齿条204就会在复位弹簧一206的作用下进行复位,即双向齿条204沿着竖直导向杆205向上滑动,同时向上移动的还有套印模具210和驱动架212,在双向齿条204向上移动的时候,双向齿条204会推动复位弹簧一206进行方向转动,此时形成棘轮棘爪配合的限位棘轮208与传动轴209就会使传动轴209带动皮带组件301进行转动。When the
当皮带组件301进行转动的时候,与皮带组件301形成带轮配合的水平轴302就会转动,那么圆锥齿轮组303就会随着水平轴302一起转动,使圆锥齿轮组303带动传送带304转动,这样向前转动的传送带304就会将下一个待套印的加工件8向前输送到套印模具210的下方,同时将刚完成套印的加工件8向前输送到压合头603下方。When the
具体地,待套印的加工件8到达的传送带304上的过程为,在套印模具210向下移动对上一个加工件8完成套印的过程中,存在两个挤压板404向相互靠近方向移动的过程,在挤压板404移动的过程中,固定安装在挤压板404上的推杆501也会移动,那么推杆501就会沿着球头杆502上的球发生滑动,并且由于推杆501是倾斜布置的状态,所以推杆501就会推动球头杆502沿着导向架506滑动,滑动的方向为球头杆502逐渐靠近储料筒505,这个过程中复位弹簧四503会被压缩,复位弹簧四503的作用是辅助球头杆502复位。由于球头杆502与三脚架504固定连接,所以三脚架504也会移动,并且三脚架504上斜面的一侧朝向储料筒505,所以三脚架504滑进储料筒505中并将一个加工件8从下料机构5中推出到传送带304上的夹持架7中,完成一次送料。在套印模具210向上移动的过程中,挤压板404向相互远离的方向滑动,推杆501和三脚架504复位,三脚架504从储料筒505中滑出。这样就完成了送料。Specifically, the process that the
电机201在工作过程中会产生热量,而产生的热量就会存储在外箱601中,由于外箱601与导热管602连通,所以热量会通过导热管602到达压合头603,从压合头603中流出,在电机201和驱动架212向下移动的过程中,驱动架212会向下推动滑动板605,使滑动板605沿着U形导向杆606向下滑动的同时将压合头603向下压,压合头603从导热管602中滑出,并拉伸复位弹簧五604,向下移动的压合头603将上一个完成套印的加工件8套住,即在套印模具210对一个新的加工件8进行套印的时候,压合头603就会对上一个完成套印的加工件8进行加热,对加工件8的表面进行烘干,这个过程中,复位弹簧五604的作用是辅助压合头603和滑动板605的复位。The
需要说明的是,圆锥齿轮组303包括了一个主动圆锥齿轮和一个从动圆锥齿轮,主动圆锥齿轮作为输入端与水平轴302固定连接,从动圆锥齿轮作为输出端与传送带304上的转轴固定连接。同时,皮带组件301包括一个皮带和两个带轮,两个带轮分别与水平轴302和传动轴209固定连接,两个带轮通过皮带连接,这对于本领域技术人员而言是可以想到的。It should be noted that the bevel gear set 303 includes a driving bevel gear and a driven bevel gear, the driving bevel gear is fixedly connected to the
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211538982.0A CN116252539A (en) | 2022-12-02 | 2022-12-02 | Fluorocarbon paint overprinting technology positioner |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202211538982.0A CN116252539A (en) | 2022-12-02 | 2022-12-02 | Fluorocarbon paint overprinting technology positioner |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN116252539A true CN116252539A (en) | 2023-06-13 |
Family
ID=86678257
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202211538982.0A Pending CN116252539A (en) | 2022-12-02 | 2022-12-02 | Fluorocarbon paint overprinting technology positioner |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN116252539A (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN118237568A (en) * | 2024-05-28 | 2024-06-25 | 泰州市天元精密铸造有限公司 | Metal hardware casting forming device |
-
2022
- 2022-12-02 CN CN202211538982.0A patent/CN116252539A/en active Pending
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN118237568A (en) * | 2024-05-28 | 2024-06-25 | 泰州市天元精密铸造有限公司 | Metal hardware casting forming device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| WO2022227747A1 (en) | Express delivery label printing device in logistics and transportation | |
| CN206999915U (en) | Pcb board laser marking machine | |
| CN203919960U (en) | A kind of UV ink printing equipment | |
| CN203568398U (en) | Automatic feeding device | |
| CN220429583U (en) | A screen printing device for a thermos cup | |
| CN103332018B (en) | Printer for printing characters on surfaces of pencils | |
| CN104249550A (en) | Automatic printing equipment | |
| CN116207018A (en) | Stacked equipment of semiconductor lead frame | |
| CN110843324A (en) | Screen printing device and method for photovoltaic panel | |
| CN110052717B (en) | Tracking type dynamic bottle cap marking device | |
| CN103085447B (en) | High rotating type printing machine and rotating type printing method thereof | |
| CN211106195U (en) | Automatic printing device for cosmetic bottle | |
| CN204504025U (en) | Dial mechanism of bending machine | |
| CN209649457U (en) | A kind of battery rubber shell automatic word pressing machine | |
| CN110064847A (en) | A kind of tracking mode dynamic bottle cap marking method | |
| CN116387205A (en) | A fully automated assembly and production equipment for Bluetooth headset chips | |
| CN204725996U (en) | A kind of printing equipment | |
| CN116544159A (en) | Eutectic chip mounter with turret type bonding head | |
| CN110039185B (en) | Laser coding equipment for rotary bottle cap | |
| CN214215113U (en) | Efficient screen printing machine for plastic packaging container | |
| CN223355208U (en) | A printing device for carton | |
| CN222571851U (en) | Packing carton printing device convenient to change printing roller | |
| CN219131139U (en) | Laser printer | |
| US3892400A (en) | Paper feeder means for printing press | |
| CN220314527U (en) | A kind of product outer packaging printing device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20230613 |