CN115923112B - Stretching equipment for BOPP film - Google Patents
Stretching equipment for BOPP film Download PDFInfo
- Publication number
- CN115923112B CN115923112B CN202310218676.7A CN202310218676A CN115923112B CN 115923112 B CN115923112 B CN 115923112B CN 202310218676 A CN202310218676 A CN 202310218676A CN 115923112 B CN115923112 B CN 115923112B
- Authority
- CN
- China
- Prior art keywords
- column
- fixedly installed
- plate
- stretching
- unit
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Shaping By String And By Release Of Stress In Plastics And The Like (AREA)
Abstract
本发明涉及BOPP薄膜拉伸技术领域,具体为一种BOPP薄膜用拉伸设备,包括输送单元、拉伸单元与收卷单元,所述输送单元上固定安装有拉伸单元,拉伸单元下端固定安装有收卷单元。本发明通过输送单元对流延机加工出的厚片进行压平输送,使其顺利进入拉伸单元,通过拉伸单元对厚片进行同步双向拉伸处理,拉伸前,通过增加额外的接触点来增加厚片的拉伸点,从而使拉伸后的薄膜边缘变形点增多,从而减小薄膜边缘变形的宽度,减小薄膜边缘所要切除的宽度,从而提高设备的加工利用率,通过收卷单元对薄膜进行收卷,且可快速将收卷完成的薄膜与设备分离,从而缩短设备停止工作的时间,提高设备的加工效率。
The invention relates to the technical field of BOPP film stretching, in particular to a stretching device for BOPP film, comprising a conveying unit, a stretching unit and a winding unit, a stretching unit is fixedly installed on the conveying unit, and the lower end of the stretching unit is fixed A winding unit is installed. In the present invention, the thick sheet processed by the tape casting machine is flattened and conveyed through the conveying unit, so that it enters the stretching unit smoothly, and the thick sheet is synchronously bidirectionally stretched through the stretching unit. Before stretching, by adding additional contact points To increase the stretch point of the thick film, so that the stretched film edge deformation point increases, thereby reducing the width of the film edge deformation, reducing the width of the film edge to be cut, thereby improving the processing utilization of the equipment, through winding The unit rewinds the film, and can quickly separate the rewound film from the equipment, thereby shortening the time for the equipment to stop working and improving the processing efficiency of the equipment.
Description
技术领域technical field
本发明涉及BOPP薄膜拉伸技术领域,具体为一种BOPP薄膜用拉伸设备。The invention relates to the technical field of BOPP film stretching, in particular to a stretching device for BOPP film.
背景技术Background technique
BOPP薄膜是一种优良透明软包装材料,其是由聚丙烯颗粒经共挤形成片材后,再经纵横两个方向的拉伸制作而成,BOPP薄膜具有质轻、无毒、无臭、防潮、使用范围广,以及性能稳定、生产高效节能等优势,并且总厚度降低,BOPP薄膜的主要加工方式是平膜法,平膜法分为同步双向拉伸法及逐步双向拉伸法,这里主要针对同步双向拉伸法加工BOPP薄膜。BOPP film is an excellent transparent flexible packaging material. It is made of polypropylene particles that are co-extruded to form a sheet, and then stretched in both vertical and horizontal directions. BOPP film is light, non-toxic, odorless, and moisture-proof. , a wide range of applications, stable performance, high efficiency and energy saving in production, and reduced total thickness. The main processing method of BOPP film is the flat film method. The flat film method is divided into synchronous biaxial stretching method and stepwise biaxial stretching method. Processing of BOPP films for simultaneous biaxial stretching.
同步双向拉伸法是将经过流延机加工出的厚片送入拉伸设备处进行同时纵横两个方向的拉伸,拉伸后的薄膜拉伸处边缘变形,无法使用,因此需要在收卷前对其进行切割处理,由于同步双向拉伸法拉伸薄膜时,需要进行双向拉伸,但因薄膜的拉伸接触点较少,导致薄膜边缘变形量大,造成薄膜后续切割废料的尺寸较大,薄膜的浪费率和生产成本高,且薄膜收卷完成后,需要将其取下,然后重新套设上收卷零件,导致设备需要停止工作一段时间,使设备的加工效率降低。The synchronous bidirectional stretching method is to send the thick film processed by the tape casting machine to the stretching equipment for simultaneous stretching in both vertical and horizontal directions. After stretching, the edge of the stretched film is deformed and cannot be used. It is cut before rolling, because when the film is stretched by the synchronous biaxial stretching method, biaxial stretching is required, but because the stretching contact points of the film are small, the edge deformation of the film is large, resulting in the size of the waste material after cutting the film Larger, the waste rate and production cost of the film are high, and after the film winding is completed, it needs to be removed, and then the upper winding part is re-installed, causing the equipment to stop working for a period of time, reducing the processing efficiency of the equipment.
发明内容Contents of the invention
为了解决上述技术问题,本发明提供一种BOPP薄膜用拉伸设备。In order to solve the above technical problems, the present invention provides a stretching device for BOPP film.
一种BOPP薄膜用拉伸设备,包括输送单元、拉伸单元与收卷单元,所述输送单元上固定安装有拉伸单元,拉伸单元下端固定安装有收卷单元。A stretching device for BOPP film, comprising a conveying unit, a stretching unit and a winding unit, a stretching unit is fixedly installed on the conveying unit, and a winding unit is fixedly installed at the lower end of the stretching unit.
所述拉伸单元包括烘箱,输送单元上固定安装有烘箱,烘箱内部前后对称固定安装有电动推杆,电动推杆末端均固定安装有左夹紧架,左夹紧架右端固定安装有右夹紧架,烘箱下侧转动连接有送料架。The stretching unit includes an oven, an oven is fixedly installed on the conveying unit, an electric push rod is fixedly installed symmetrically front and rear inside the oven, the end of the electric push rod is fixedly installed with a left clamping frame, and the right end of the left clamping frame is fixedly installed with a right clamping frame. Tight frame, the lower side of the oven is rotatably connected with a feeding frame.
所述收卷单元包括固定立板,烘箱下端固定安装有固定立板,固定立板前端转动连接有收卷辊,固定立板后端通过电机座固定安装有电机一,电机一输出轴通过联轴器与收卷辊固定连接,固定立板前端转动连接有双向螺纹杆,双向螺纹杆前后两侧开设有旋向相反的螺纹槽,双向螺纹杆前后对称以螺纹连接的方式连接有切割刀,固定立板前端固定安装有贯穿切割刀的导向杆。The rewinding unit includes a fixed vertical plate, the lower end of the oven is fixedly installed with a fixed vertical plate, the front end of the fixed vertical plate is rotatably connected with a winding roller, the rear end of the fixed vertical plate is fixedly installed with a motor 1 through a motor seat, and the output shaft of the motor 1 passes through a coupling. The shaft device is fixedly connected with the winding roller, and the front end of the fixed vertical plate is connected with a two-way threaded rod. The front and rear sides of the two-way threaded rod are provided with thread grooves with opposite rotation directions. The front end of the fixed vertical plate is fixedly equipped with a guide rod that runs through the cutting knife.
优选技术方案一:所述输送单元包括工作台,工作台前端左右两侧对称转动连接有输送辊,输送辊后端均固定安装有齿轮一,齿轮一相啮合,工作台后端通过电机座固定安装有电机二,电机二输出轴通过联轴器与左侧的齿轮一固定连接,输送辊中部转动连接有螺纹柱,螺纹柱上以螺纹连接的方式连接有小径端水平向后的圆台块,输送辊外端均匀开设有滑动配合槽,滑动配合槽内以滑动配合的方式连接有伸出柱,伸出柱与圆台块的倾斜面之间以滑动配合的方式相连接,伸出柱末端固定安装有定位支架,定位支架上转动连接有挤压柱。Optimum technical solution 1: the conveying unit includes a workbench, the front end of the workbench is connected with conveying rollers symmetrically rotating on the left and right sides, the rear end of the conveying rollers is fixedly equipped with gear one, and the gear one meshes with each other, and the rear end of the workbench is fixed by the motor seat Motor 2 is installed, and the output shaft of motor 2 is fixedly connected with gear 1 on the left side through a coupling. The middle part of the conveying roller is connected with a threaded column for rotation, and the threaded column is connected with a round table block with a small diameter end horizontally backward in a threaded manner. The outer end of the conveyor roller is uniformly provided with a sliding fitting groove, and the extending column is connected with the sliding fitting in the sliding fitting groove, and the extending column is connected with the inclined surface of the round table block in a sliding fitting manner, and the end of the extending column is fixed. A positioning bracket is installed, and an extrusion column is rotatably connected to the positioning bracket.
优选技术方案二:所述烘箱包括矩形板,矩形板中部开设有矩形通孔,左夹紧架上端固定安装有导向块,矩形板内壁固定安装有网格管道,网格管道上均匀固定安装有贯穿矩形板的锥形出气口,烘箱右端固定安装有气泵,气泵右端固定安装有螺纹形进气管,螺纹形进气管进气口固定安装有过滤板,螺纹形进气管外端固定安装有保温套,保温套内固定安装有电热丝。Optimal technical solution 2: the oven includes a rectangular plate, a rectangular through hole is opened in the middle of the rectangular plate, a guide block is fixedly installed on the upper end of the left clamping frame, a grid pipe is fixedly installed on the inner wall of the rectangular plate, and a grid pipe is evenly fixed on the grid pipe. The tapered air outlet runs through the rectangular plate, the right end of the oven is fixed with an air pump, the right end of the air pump is fixed with a threaded air intake pipe, the air inlet of the threaded air intake pipe is fixed with a filter plate, and the outer end of the threaded air intake pipe is fixed with an insulation cover , The heating wire is fixedly installed in the insulation cover.
优选技术方案三:所述左夹紧架包括控制板,电动推杆末端均固定安装有控制板,控制板相对端均以上下滑动配合的方式连接有左夹紧柱,最中部的左夹紧柱与控制板固定连接, 相邻的左夹紧柱中部共同均铰接有V形铰接杆, V形铰接杆由两个同轴心转动连接的杆身组成, V形铰接杆中部靠近控制板一端转动连接有连接杆,连接杆共同以滑动配合的方式连接有矩形连接板,控制板中部固定安装有电动伸缩杆,电动伸缩杆末端与矩形连接板固定连接,左夹紧柱右端固定安装有磁吸块,相邻的左夹紧柱之间共同固定连接有可伸缩支撑柱一,可伸缩支撑柱一右端与磁吸块右端对齐。Optimum technical solution 3: the left clamping frame includes a control panel, and the control panel is fixedly installed at the end of the electric push rod, and the opposite end of the control panel is connected with the left clamping column in the way of sliding fit up and down, and the left clamping column in the middle is The column is fixedly connected with the control panel, and the middle part of the adjacent left clamping column is jointly hinged with a V-shaped hinged rod. The V-shaped hinged rod is composed of two shafts connected by rotation with the same axis. The middle part of the V-shaped hinged rod is close to one end of the control board. The connecting rods are rotatably connected with a rectangular connecting plate in a sliding fit, the middle of the control panel is fixedly installed with an electric telescopic rod, the end of the electric telescopic rod is fixedly connected with the rectangular connecting plate, and the right end of the left clamping column is fixedly installed with a magnetic The suction block and the adjacent left clamping columns are jointly fixedly connected with a telescopic support column 1, and the right end of the telescopic support column 1 is aligned with the right end of the magnetic suction block.
优选技术方案四:所述右夹紧架包括夹紧气缸, 控制板右端固定安装有夹紧气缸, 夹紧气缸右端固定安装有倒Z形板, 倒Z形板相对端均以滑动配合的方式连接有右夹紧柱,右夹紧柱均匀排布,中部的右夹紧柱与倒Z形板固定连接,右夹紧柱左端固定安装有电磁板,电磁板与磁吸块外端均开设有圆角,右夹紧柱之间共同固定连接有可伸缩支撑柱二, 可伸缩支撑柱二左端与电磁板左端对齐。Preferred technical solution four: the right clamping frame includes a clamping cylinder, the right end of the control panel is fixedly installed with a clamping cylinder, the right end of the clamping cylinder is fixedly installed with an inverted Z-shaped plate, and the opposite ends of the inverted Z-shaped plate are all in a sliding fit The right clamping column is connected with the right clamping column, and the right clamping column is evenly arranged. The right clamping column in the middle is fixedly connected with the inverted Z-shaped plate, and the left end of the right clamping column is fixedly installed with an electromagnetic plate. There are rounded corners, and the right clamping columns are jointly fixedly connected with the second telescopic support column, and the left end of the second telescopic support column is aligned with the left end of the electromagnetic plate.
优选技术方案五:所述送料架包括送料柱一, 烘箱内部下侧转动连接有送料柱一, 烘箱内部且位于送料柱一右侧转动连接有送料柱二, 送料柱一与送料柱二后端均固定安装有齿轮二,齿轮二相啮合,右侧的齿轮二后端固定安装有链轮一, 收卷辊后侧固定安装有链轮二,链轮一与链轮二之间通过齿链带传动连接。Optimum technical solution five: the feeding frame includes a feeding column 1, a feeding column 1 is rotatably connected to the lower side inside the oven, and a feeding column 2 is rotatably connected to the inside of the oven and located on the right side of the feeding column 1, and the rear end of the feeding column 1 and the feeding column 2 are rotatably connected. Both gears are fixedly installed with the second gear, and the second gear is meshed. The rear end of the second gear on the right is fixed with the first sprocket, and the rear side of the winding roller is fixed with the second sprocket. Belt drive connection.
优选技术方案六:所述收卷辊上套设有工字筒,工字筒表面贴有双面胶布,收卷辊前侧以螺纹连接的方式连接有旋紧螺杆,旋紧螺杆位于收卷辊中轴线左侧,旋紧螺杆前端固定安装有紧压板, 紧压板的长度小于旋紧螺杆中轴线与收卷辊外缘的最大距离。Optimum technical solution six: the winding roller is covered with an I-shaped cylinder, the surface of the I-shaped cylinder is pasted with double-sided adhesive tape, and the front side of the winding roller is connected with a tightening screw in a threaded manner. On the left side of the central axis of the roller, a tightening plate is fixedly installed at the front end of the tightening screw, and the length of the tightening plate is less than the maximum distance between the central axis of the tightening screw and the outer edge of the winding roller.
优选技术方案七:所述切割刀包括L形弯刀, 双向螺纹杆前后对称以螺纹连接的方式连接有L形弯刀,L形弯刀上端开设有倒角导料倒角。Optimum technical solution 7: the cutting knife includes an L-shaped machete, the L-shaped machete is connected to the two-way threaded rod symmetrically in a threaded manner, and the upper end of the L-shaped machete is provided with a chamfering guide chamfer.
优选技术方案八:所述可伸缩支撑柱一包括方形柱一,相邻的左夹紧柱的相对端均固定连接有方形柱一,方形柱一中部外端以滑动配合的方式连接有方形框板一,方形框板一中部以滑动配合的方式连接有方形移动块一,方形移动块一之间、方形移动块一与方形柱一之间均固定安装有圆柱弹簧,方形框板一右端固定安装有挤压半球,挤压半球右端与磁吸块右端齐平。Optimum technical solution eight: the telescopic support column 1 includes a square column 1, the opposite ends of the adjacent left clamping columns are fixedly connected to the square column 1, and the outer end of the middle part of the square column 1 is connected to a square frame in a sliding fit Plate 1, the middle part of the square frame plate 1 is connected with a square moving block 1 in a sliding fit, cylindrical springs are fixedly installed between the square moving blocks 1, between the square moving block 1 and the square column 1, and the right end of the square frame plate 1 is fixed An extrusion hemisphere is installed, and the right end of the extrusion hemisphere is flush with the right end of the magnetic block.
本发明具备以下有益效果:1、本发明提供的一种BOPP薄膜用拉伸设备,通过输送单元对流延机加工出的厚片进行压平输送,使其顺利进入拉伸单元,通过拉伸单元对厚片进行同步双向拉伸处理,拉伸前,通过增加额外的接触点来增加厚片的拉伸点,从而使拉伸后的薄膜边缘变形点增多,从而减小薄膜边缘变形的宽度,减小薄膜边缘所要切除的宽度,从而提高设备的加工利用率,通过收卷单元对薄膜进行收卷,且可快速将收卷完成的薄膜与设备分离,从而缩短设备停止工作的时间,提高设备的加工效率。The present invention has the following beneficial effects: 1. A kind of stretching equipment for BOPP film provided by the present invention, through the conveying unit, the thick sheet processed by the tape casting machine is flattened and conveyed, so that it enters the stretching unit smoothly, and passes through the stretching unit Perform synchronous biaxial stretching on the thick film. Before stretching, increase the stretching point of the thick film by adding additional contact points, so that the edge deformation points of the stretched film will increase, thereby reducing the width of the film edge deformation. Reduce the width to be cut off at the edge of the film, thereby improving the processing utilization of the equipment. The film is rewound through the rewinding unit, and the rewound film can be quickly separated from the equipment, thereby shortening the time for the equipment to stop working and improving the equipment. processing efficiency.
2、本发明设置的输送单元,通过转动螺纹柱改变圆台块的位置,从而改变伸出柱的伸出长度,使挤压柱与厚片之间紧贴,以达到对厚片的挤压与输送的目的,保证厚片进入拉伸单元时处于平整状态,降低拉伸单元对厚片进行拉伸时的难度。2. The conveying unit provided by the present invention changes the position of the round table block by rotating the threaded column, thereby changing the extension length of the extended column, so that the extruding column and the slab are in close contact, so as to achieve the extrusion of the slab and the The purpose of conveying is to ensure that the thick sheet is in a flat state when it enters the stretching unit, and to reduce the difficulty of stretching the thick sheet by the stretching unit.
3、本发明设置的拉伸单元,通过过滤板防止气体中含有杂质而污染薄膜表面,影响薄膜质量,通过保温套避免电热丝产生的热量与外界接触,从而导致热量散失,增加加工成本。3. The stretching unit provided by the present invention prevents impurities in the gas from polluting the surface of the film through the filter plate, affecting the quality of the film, and prevents the heat generated by the heating wire from contacting the outside world through the insulation cover, thereby causing heat loss and increasing processing costs.
4、本发明设置的拉伸单元,通过可伸缩支撑柱一对相邻的左夹紧柱之间的厚片进行分点定位,从而在不增多左夹紧柱的情况下,增加对厚片进行夹紧定位的点的数目,保证厚片经过拉伸后的变形点之间的形变量减小,从而减小薄膜边缘所要切除的宽度,降低薄膜加工过程中产生的废料的量,提高装置加工薄膜的利用率。4. The stretching unit provided in the present invention uses telescopic support columns to position the slabs between a pair of adjacent left clamping columns in points, thereby increasing the thickness of the slabs without increasing the number of left clamping columns. The number of points for clamping and positioning ensures that the deformation between the deformation points of the thick sheet after stretching is reduced, thereby reducing the width to be cut off the edge of the film, reducing the amount of waste generated during film processing, and improving the device. Utilization of processed films.
5、本发明设置的收卷单元,通过转动旋紧螺杆控制紧压板来实现工字筒和收卷辊之间的相对固定,从而定位工字筒或者快速拆卸工字筒,通过挤压半球对厚片进行挤压定位,通过圆柱弹簧保证方形框板一均匀的分布于左夹紧柱之间,使左夹紧柱之间的厚片受力均匀。5. The winding unit provided in the present invention realizes the relative fixation between the I-shaped cylinder and the winding roller by rotating and tightening the screw to control the pressing plate, so as to position the I-shaped cylinder or quickly disassemble the I-shaped cylinder. The slab is squeezed and positioned, and the square frame plate is evenly distributed between the left clamping columns through the cylindrical spring, so that the slab between the left clamping columns is evenly stressed.
附图说明Description of drawings
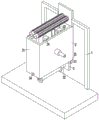
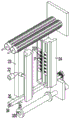
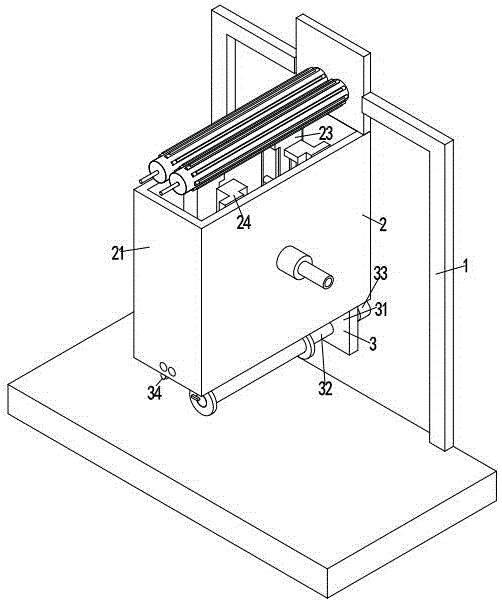
图1为本发明的主视立体结构示意图。FIG. 1 is a schematic diagram of a front-view stereoscopic structure of the present invention.
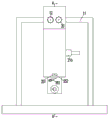
图2为本发明的主视平面结构示意图。Fig. 2 is a schematic diagram of the front view plane structure of the present invention.
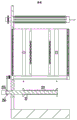
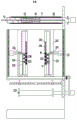
图3为本发明的图2的A-A向的剖视图。Fig. 3 is a cross-sectional view along the line A-A of Fig. 2 of the present invention.
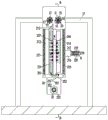
图4为本发明的主视局部剖视平面结构示意图。Fig. 4 is a schematic plan view of a partial cross-sectional plan view of the present invention.
图5为本发明的图4的B-B向的剖视图。Fig. 5 is a sectional view along the B-B direction of Fig. 4 of the present invention.
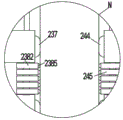
图6为本发明的图4的N处的局部放大图。FIG. 6 is a partial enlarged view of N in FIG. 4 of the present invention.
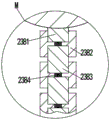
图7为本发明的图5的M处的局部放大图。FIG. 7 is a partially enlarged view of the M in FIG. 5 of the present invention.
图8为本发明的后视平面结构示意图。Fig. 8 is a schematic diagram of the rear view plane structure of the present invention.
图9为本发明的左夹紧架与右夹紧架的主视立体结构示意图。FIG. 9 is a schematic perspective view of the left clamping frame and the right clamping frame of the present invention.
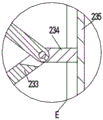
图10为本发明的图5的E处的局部放大图。FIG. 10 is a partial enlarged view at E of FIG. 5 of the present invention.
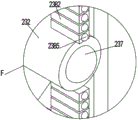
图11为本发明的图9的F处的局部放大图。FIG. 11 is a partial enlarged view at F of FIG. 9 of the present invention.
图12为本发明的图4的G处的局部放大图。FIG. 12 is a partial enlarged view of G in FIG. 4 of the present invention.
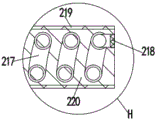
图13为本发明的图4的H处的局部放大图。FIG. 13 is a partial enlarged view of H in FIG. 4 of the present invention.
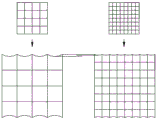
图14为本发明可伸缩支撑柱一与可伸缩支撑柱二使用前后的薄膜状态对比图。Fig. 14 is a comparison diagram of the film state before and after use of the first telescopic support column and the second telescopic support column of the present invention.
图中:1、输送单元;11、工作台;12、输送辊;13、齿轮一;14、电机二;15、螺纹柱;16、圆台块;17、滑动配合槽;18、伸出柱;19、定位支架;20、挤压柱;2、拉伸单元;21、烘箱;211、矩形板;212、矩形通孔;213、导向块;214、网格管道;215、锥形出气口;216、气泵;217、螺纹形进气管;218、过滤板;219、保温套;220、电热丝;22、电动推杆;23、左夹紧架;231、控制板;232、左夹紧柱;233、V形铰接杆;234、连接杆;235、矩形连接板;236、电动伸缩杆;237、磁吸块;238、可伸缩支撑柱一;2381、方形柱一;2382、方形框板一;2383、方形移动块一;2384、圆柱弹簧;2385、挤压半球;24、右夹紧架;241、夹紧气缸;242、倒Z形板;243、右夹紧柱;244、电磁板;245、可伸缩支撑柱二;25、送料架;251、送料柱一;252、送料柱二;253、齿轮二;254、链轮一;255、链轮二;256、齿链带;3、收卷单元;31、固定立板;32、收卷辊;321、工字筒;322、双面胶布;323、旋紧螺杆;324、紧压板;33、电机一;34、双向螺纹杆;35、切割刀;351、L形弯刀;352、导料倒角;36、导向杆。In the figure: 1, conveying unit; 11, working table; 12, conveying roller; 13, gear 1; 14, motor 2; 15, threaded column; 16, round table block; 17, sliding fit groove; 19. Positioning bracket; 20. Extrusion column; 2. Stretching unit; 21. Oven; 211. Rectangular plate; 212. Rectangular through hole; 213. Guide block; 216, air pump; 217, threaded intake pipe; 218, filter plate; 219, heat preservation cover; 220, heating wire; 22, electric push rod; 23, left clamping frame; 231, control panel; 232, left clamping
实施方式Implementation
下面将结合本发明实施例中的附图,对本发明实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本发明一部分实施例,而不是全部的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本发明保护的范围。The following will clearly and completely describe the technical solutions in the embodiments of the present invention with reference to the accompanying drawings in the embodiments of the present invention. Obviously, the described embodiments are only some, not all, embodiments of the present invention. Based on the embodiments of the present invention, all other embodiments obtained by persons of ordinary skill in the art without making creative efforts belong to the protection scope of the present invention.
参阅图1,一种BOPP薄膜用拉伸设备,包括输送单元1、拉伸单元2与收卷单元3,所述输送单元1上固定安装有拉伸单元2,拉伸单元2下端固定安装有收卷单元3。Referring to Fig. 1, a kind of stretching equipment for BOPP film, comprises conveying unit 1, stretching unit 2 and winding unit 3, described conveying unit 1 is fixedly installed with stretching unit 2, and the lower end of stretching unit 2 is fixedly installed with Winding unit 3.
参阅图1与图9,所述拉伸单元2包括烘箱21,输送单元1上固定安装有烘箱21,烘箱21内部前后对称固定安装有电动推杆22,电动推杆22末端均固定安装有左夹紧架23,左夹紧架23右端固定安装有右夹紧架24,烘箱21下侧转动连接有送料架25;首先将来自流延机的厚片通过输送单元1输送至烘箱21内,通过烘箱21对厚片进行加热,使其达到拉伸温度,此时通过左夹紧架23与右夹紧架24对厚片进行夹紧处理,并对厚片进行横向与纵向的拉伸,通过送料架25对拉伸后的薄膜进行压平与输送处理。Referring to Fig. 1 and Fig. 9, the stretching unit 2 includes an
继续参阅图1、图4、图5与图9,所述收卷单元3包括固定立板31,烘箱21下端固定安装有固定立板31,固定立板31前端转动连接有收卷辊32,固定立板31后端通过电机座固定安装有电机一33,电机一33输出轴通过联轴器与收卷辊32固定连接,固定立板31前端转动连接有双向螺纹杆34,双向螺纹杆34前后两侧开设有旋向相反的螺纹槽,双向螺纹杆34前后对称以螺纹连接的方式连接有切割刀35,固定立板31前端固定安装有贯穿切割刀35的导向杆36;经过压平处理后的薄膜输送至收卷辊32上并进行定位,根据左夹紧架23与右夹紧架24的最终拉伸位置,调整切割刀35之间的距离,使切割刀35之间的距离与最终拉伸时的左夹紧架23之间的距离相同,右夹紧架24之间的距离始终和左夹紧架23之间的距离相等,通过切割刀35对薄膜拉伸变形后的边缘进行切割,通过电机一33带动收卷辊32转动,对经过切割处理后的薄膜进行收卷。Continue to refer to Fig. 1, Fig. 4, Fig. 5 and Fig. 9, the rewinding unit 3 includes a fixed
参阅图4、图5、图8与图12,所述输送单元1包括工作台11,工作台11前端左右两侧对称转动连接有输送辊12,输送辊12后端均固定安装有齿轮一13,齿轮一13相啮合,工作台11后端通过电机座固定安装有电机二14,电机二14输出轴通过联轴器与左侧的齿轮一13固定连接,输送辊12中部转动连接有螺纹柱15,螺纹柱15上以螺纹连接的方式连接有小径端水平向后的圆台块16,输送辊12外端均匀开设有滑动配合槽17,滑动配合槽17内以滑动配合的方式连接有伸出柱18,伸出柱18与圆台块16的倾斜面之间以滑动配合的方式相连接,伸出柱18末端固定安装有定位支架19,定位支架19上转动连接有挤压柱20;通过电机二14带动左侧的齿轮一13转动,在右侧的齿轮一13的配合下,左右两侧的输送辊12相向转动,根据输送辊12的转动速度,控制厚片的输送速度,通过转动螺纹柱15使圆台块16水平向后移动,伸出柱18在圆台块16倾斜面的作用下沿输送辊12的径向朝滑动配合槽17外部移动, 伸出柱18伸出长度增大,继而挤压柱20与输送辊12轴线之间的距离增大,使得挤压柱20可适应厚片厚度的变化并与厚片贴紧。Referring to Fig. 4, Fig. 5, Fig. 8 and Fig. 12, the conveying unit 1 includes a workbench 11, the front end of the workbench 11 is connected with conveying
参阅图4和图13,所述烘箱21包括矩形板211,矩形板211中部开设有矩形通孔212,左夹紧架23上端固定安装有导向块213,矩形板211内壁固定安装有网格管道214,网格管道214上均匀固定安装有贯穿矩形板211的锥形出气口215,烘箱21右端固定安装有气泵216,气泵216右端固定安装有螺纹形进气管217,螺纹形进气管217进气口固定安装有过滤板218,螺纹形进气管217外端固定安装有保温套219,保温套219内固定安装有电热丝220;通过气泵216将通过电热丝220加热后的气体通入网格管道214,最终通过锥形出气口215排出,通过螺纹形进气管217增加气体加热的路程,通过过滤板218防止气体中含有杂质而污染薄膜表面,通过保温套219避免电热丝220产生的热量与外界接触,从而导致热量散失,通过导向块213使厚片顺利进入左夹紧架23与右夹紧架24之间。4 and 13, the
参阅图4、图5、图9、图10与图11,所述左夹紧架23包括控制板231,电动推杆22末端均固定安装有控制板231,控制板231相对端均以上下滑动配合的方式连接有左夹紧柱232,最中部的左夹紧柱232与控制板231固定连接, 相邻的左夹紧柱232中部共同均铰接有V形铰接杆233, V形铰接杆233由两个同轴心转动连接的杆身组成,V形铰接杆233中部靠近控制板231一端转动连接有连接杆234,连接杆234共同以滑动配合的方式连接有矩形连接板235,控制板231中部固定安装有电动伸缩杆236,电动伸缩杆236末端与矩形连接板235固定连接,左夹紧柱232右端固定安装有磁吸块237,相邻的左夹紧柱232之间共同固定连接有可伸缩支撑柱一238,可伸缩支撑柱一238右端与磁吸块237右端对齐;当左夹紧架23与右夹紧架24对厚片进行夹紧后,通过电动推杆22带动控制板231相背移动,对厚片进行横向上的拉伸,同时通过电动伸缩杆236带动矩形连接板235与连接杆234相向移动,从而使V形铰接杆233的张开角度变大,使左夹紧柱232之间的距离增大, 对厚片进行纵向上的拉伸,最终达到对厚片进行横向与纵向上的同步拉伸的目的,当左夹紧柱232之间的距离增大时,可伸缩支撑柱一238的伸长长度同时增大,可伸缩支撑柱一238与左夹紧柱232同步与厚片接触,通过可伸缩支撑柱一238对相邻的左夹紧柱232之间的厚片进行分点定位,在原先左夹紧柱232所形成的定位点的数量上进一步增加定位点的数量,使厚片表面均匀分布有拉伸点,进而使得厚片受到均匀的拉伸力作用,保证厚片经过拉伸后的变形点之间的形变量减小,从而减小薄膜边缘所要切除的宽度,降低薄膜加工过程中产生的废料的量,提高装置加工薄膜的利用率。Referring to Fig. 4, Fig. 5, Fig. 9, Fig. 10 and Fig. 11, the
参阅图4、图5、图6、图9与图11,所述右夹紧架24包括夹紧气缸241, 控制板231右端固定安装有夹紧气缸241, 夹紧气缸241右端固定安装有倒Z形板242, 倒Z形板242相对端均以滑动配合的方式连接有右夹紧柱243,右夹紧柱243均匀排布,中部的右夹紧柱243与倒Z形板242固定连接,右夹紧柱243左端固定安装有电磁板244,电磁板244与磁吸块237外端均开设有圆角,右夹紧柱243之间共同固定连接有可伸缩支撑柱二245, 可伸缩支撑柱二245左端与电磁板244左端对齐;通过夹紧气缸241带动倒Z形板242朝向控制板231移动,使右夹紧柱243上的电磁板244与厚片紧贴,此时对电磁板244进行通电,使磁吸块237与电磁板244之间隔着厚片相吸,当左夹紧柱232之间的距离增大时,在磁吸块237和电磁板244相吸的情况下,左夹紧柱232可带动右夹紧柱243同步移动,可伸缩支撑柱二245与可伸缩支撑柱一238相配合同步夹紧厚片,通过上述操作对厚片进行多点夹紧定位。Referring to Fig. 4, Fig. 5, Fig. 6, Fig. 9 and Fig. 11, the
参阅图2、图3与图8,所述送料架25包括送料柱一251, 烘箱21内部下侧转动连接有送料柱一251, 烘箱21内部且位于送料柱一251右侧转动连接有送料柱二252, 送料柱一251与送料柱二252后端均固定安装有齿轮二253,齿轮二253相啮合,右侧的齿轮二253后端固定安装有链轮一254, 收卷辊32后侧固定安装有链轮二255,链轮一254与链轮二255之间通过齿链带256传动连接;通过链轮一254与链轮二255以及齿链带256的配合,以达到通过电机一33带动齿轮二253转动的目的,从而带动送料柱一251与送料柱二252相向转动,对薄膜进行压平与输送,控制其输送速度。Referring to Fig. 2, Fig. 3 and Fig. 8, the
参阅图3-5与图9,所述收卷辊32上套设有工字筒321,工字筒321表面贴有双面胶布322,收卷辊32前侧以螺纹连接的方式连接有旋紧螺杆323,旋紧螺杆323位于收卷辊32中轴线左侧,旋紧螺杆323前端固定安装有紧压板324, 紧压板324的长度小于旋紧螺杆323中轴线与收卷辊32外缘的最大距离;通过工字筒321对薄膜进行收卷,通过双面胶布322对薄膜进行定位, 初始状态下的紧压板324保持水平且整体位于收卷辊32中轴线左侧,此时紧压板324对工字筒321实施阻挡,工字筒321无法从收卷辊32取下,当工字筒321对薄膜收卷完成后,通过顺时针转动旋紧螺杆323,使紧压板324整体位于收卷辊32侧端面范围内,此时紧压板324不再对工字筒321进行阻挡, 工字筒321可顺利取下。Referring to Fig. 3-5 and Fig. 9, the winding
参阅图4,所述切割刀35包括L形弯刀351, 双向螺纹杆34前后对称以螺纹连接的方式连接有L形弯刀351,L形弯刀351上端开设有导料倒角352;通过L形弯刀351对薄膜边缘进行切割,通过导料倒角352使切割后的薄膜边缘顺利掉落,从而防止废料堆积在L形弯刀351上,影响L形弯刀351的切割。Referring to Fig. 4, described cutting knife 35 comprises L-shaped
参阅图6与图7,所述可伸缩支撑柱一238包括方形柱一2381,相邻的左夹紧柱232的相对端均固定连接有方形柱一2381,方形柱一2381中部外端以滑动配合的方式连接有方形框板一2382,方形框板一2382中部以滑动配合的方式连接有方形移动块一2383,方形移动块一2383之间、方形移动块一2383与方形柱一2381之间均固定安装有圆柱弹簧2384,方形框板一2382右端固定安装有挤压半球2385,挤压半球2385右端与磁吸块237右端齐平;通过挤压半球2385对厚片进行挤压定位,通过圆柱弹簧2384保证方形框板一2382均匀的分布于左夹紧柱232之间,使左夹紧柱232之间的厚片受力均匀。Referring to Fig. 6 and Fig. 7, the telescopic support column 1 238 includes a
具体工作时,首先将来自流延机的厚片通过输送单元1输送至烘箱21内,通过烘箱21对厚片进行加热,使其达到拉伸温度,此时通过左夹紧架23与右夹紧架24对厚片进行夹紧处理,并对厚片进行横向与纵向的拉伸,通过送料架25对拉伸后的薄膜进行压平与输送处理,经过压平处理后的薄膜输送至收卷辊32上并进行定位,根据左夹紧架23与右夹紧架24的最终拉伸位置,调整切割刀35之间的距离,使切割刀35之间的距离与左夹紧架23与右夹紧架24的最终拉伸时的距离相同,通过切割刀35对薄膜拉伸变形的边缘进行切割,通过电机一33带动收卷辊32转动,对经过切割处理后的薄膜进行收卷。During the specific work, firstly, the thick sheet from the tape casting machine is transported to the
尽管已经示出和描述了本发明的实施例,对于本领域的普通技术人员而言,可以理解在不脱离本发明的原理和精神的情况下可以对这些实施例进行多种变化、修改、替换和变型,本发明的范围由所附权利要求及其等同物限定。Although the embodiments of the present invention have been shown and described, those skilled in the art can understand that various changes, modifications and substitutions can be made to these embodiments without departing from the principle and spirit of the present invention. and modifications, the scope of the invention is defined by the appended claims and their equivalents.
Claims (5)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310218676.7A CN115923112B (en) | 2023-03-09 | 2023-03-09 | Stretching equipment for BOPP film |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202310218676.7A CN115923112B (en) | 2023-03-09 | 2023-03-09 | Stretching equipment for BOPP film |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN115923112A CN115923112A (en) | 2023-04-07 |
| CN115923112B true CN115923112B (en) | 2023-05-05 |
Family
ID=85823764
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202310218676.7A Active CN115923112B (en) | 2023-03-09 | 2023-03-09 | Stretching equipment for BOPP film |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN115923112B (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116659211B (en) * | 2023-07-28 | 2023-09-19 | 河北莫妮卡装饰材料制造有限公司 | Wallpaper processing drying device |
Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101594979A (en) * | 2007-01-23 | 2009-12-02 | 东芝机械株式会社 | Gripper Type Sheet/Film Stretching Device |
| CN102069586A (en) * | 2010-12-29 | 2011-05-25 | 汕头市远东轻化装备有限公司 | Bidirectional synchronous drawing equipment for plastic film |
| CN110065222A (en) * | 2018-01-23 | 2019-07-30 | 布鲁克纳机械有限责任两合公司 | Equipment for uniaxial or biaxial stretching plastic material segment |
| CN111422457A (en) * | 2020-04-01 | 2020-07-17 | 广州市瑞扬机械设备有限公司 | Servo type abnormal bottle label supporting mechanism |
| CN112192832A (en) * | 2020-09-21 | 2021-01-08 | 广州市普同实验分析仪器有限公司 | Film stretching device |
| CN112397421A (en) * | 2020-11-16 | 2021-02-23 | 太仓联科工业设计有限公司 | Automatic film pasting equipment for surface of semiconductor wafer |
| CN112936834A (en) * | 2021-01-27 | 2021-06-11 | 山东森荣新材料股份有限公司 | Bidirectional stretching equipment for producing PTFE (polytetrafluoroethylene) ultra-precise filtering membrane |
| CN113733534A (en) * | 2021-09-30 | 2021-12-03 | 广州市普同实验分析仪器有限公司 | Film stretcher |
| CN113844943A (en) * | 2021-10-27 | 2021-12-28 | 天津市华恒包装材料有限公司 | Preparation process of BOPP heat-sealing film for packaging bag |
| CN215473063U (en) * | 2021-09-01 | 2022-01-11 | 江苏世恒医疗科技有限公司 | Production PE membrane rapid stretching device |
| CN115416272A (en) * | 2022-09-16 | 2022-12-02 | 华瑞达包装材料股份有限公司 | Stretching device is used in production of BOPP film |
-
2023
- 2023-03-09 CN CN202310218676.7A patent/CN115923112B/en active Active
Patent Citations (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101594979A (en) * | 2007-01-23 | 2009-12-02 | 东芝机械株式会社 | Gripper Type Sheet/Film Stretching Device |
| CN102069586A (en) * | 2010-12-29 | 2011-05-25 | 汕头市远东轻化装备有限公司 | Bidirectional synchronous drawing equipment for plastic film |
| CN110065222A (en) * | 2018-01-23 | 2019-07-30 | 布鲁克纳机械有限责任两合公司 | Equipment for uniaxial or biaxial stretching plastic material segment |
| CN111422457A (en) * | 2020-04-01 | 2020-07-17 | 广州市瑞扬机械设备有限公司 | Servo type abnormal bottle label supporting mechanism |
| CN112192832A (en) * | 2020-09-21 | 2021-01-08 | 广州市普同实验分析仪器有限公司 | Film stretching device |
| CN112397421A (en) * | 2020-11-16 | 2021-02-23 | 太仓联科工业设计有限公司 | Automatic film pasting equipment for surface of semiconductor wafer |
| CN112936834A (en) * | 2021-01-27 | 2021-06-11 | 山东森荣新材料股份有限公司 | Bidirectional stretching equipment for producing PTFE (polytetrafluoroethylene) ultra-precise filtering membrane |
| CN215473063U (en) * | 2021-09-01 | 2022-01-11 | 江苏世恒医疗科技有限公司 | Production PE membrane rapid stretching device |
| CN113733534A (en) * | 2021-09-30 | 2021-12-03 | 广州市普同实验分析仪器有限公司 | Film stretcher |
| CN113844943A (en) * | 2021-10-27 | 2021-12-28 | 天津市华恒包装材料有限公司 | Preparation process of BOPP heat-sealing film for packaging bag |
| CN115416272A (en) * | 2022-09-16 | 2022-12-02 | 华瑞达包装材料股份有限公司 | Stretching device is used in production of BOPP film |
Also Published As
| Publication number | Publication date |
|---|---|
| CN115923112A (en) | 2023-04-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN112793138A (en) | Gear transmission type film synchronous biaxial stretching device and matched process method thereof | |
| CN115923112A (en) | A kind of stretching equipment for BOPP film | |
| CN115284596A (en) | High accuracy toughened glass laminating machine | |
| CN118683786A (en) | A kind of veterinary medicine vacuum sealing packaging equipment and method | |
| CN218256781U (en) | Luggage plastic sheet surface coating device | |
| CN212608588U (en) | A cutting device for packaging bag production | |
| CN112277326A (en) | A compression fittings for production of PVC coiled material | |
| CN219151717U (en) | An amorphous strip shearing device | |
| CN211590303U (en) | A device for pre-grooving core material of vacuum insulation board | |
| CN114851529A (en) | Bidirectional stretching multifunctional mechanism of antifogging film with high heat-sealing strength | |
| CN221809397U (en) | A horizontal and vertical slitting machine for film material processing | |
| CN220052056U (en) | Cutting device with limit function | |
| WO2021146825A1 (en) | Continuous cutting apparatus for plastic film machining | |
| CN118544606B (en) | Automotive glass PVB intermediate coat former | |
| CN115556157A (en) | Fixed-length cutting equipment for separating metal foil from plated metal film | |
| CN220030403U (en) | Cutter is used in production of silence bubble cotton gum | |
| CN216807527U (en) | Mask cover automation equipment | |
| CN221890664U (en) | Cambered surface forming device is used in aluminium veneer production | |
| CN210908314U (en) | Adjustable pipe cutting machine for heat pipe production | |
| CN112720611A (en) | Cutting positioning device for plastic film production | |
| CN222844811U (en) | A laminating machine with limiting function | |
| CN110758851A (en) | An automatic adjustment side baffle device | |
| CN213107242U (en) | Novel circular knife waste discharge device | |
| CN224116707U (en) | A film coating device for processing color steel rock wool sandwich panels | |
| CN223099951U (en) | Screen laminating device for liquid crystal display television production |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address |
Address after: No. 500, Qingsan Street, Central District, Binhai New Area Economic and Technological Development Zone, Tianjin 300272 Patentee after: Tianjin Huaheng New Materials Co.,Ltd. Country or region after: China Address before: 300450 1-4, No. 1, Fangsi Road, light textile economic zone, Binhai New Area, Tianjin (centralized office area) Patentee before: TIANJIN HUAHENG PACKAGING MATERIALS Co.,Ltd. Country or region before: China |
|
| CP03 | Change of name, title or address |