CN112051054A - Gear positioning device, gear measuring device and measuring method - Google Patents
Gear positioning device, gear measuring device and measuring method Download PDFInfo
- Publication number
- CN112051054A CN112051054A CN202010867617.9A CN202010867617A CN112051054A CN 112051054 A CN112051054 A CN 112051054A CN 202010867617 A CN202010867617 A CN 202010867617A CN 112051054 A CN112051054 A CN 112051054A
- Authority
- CN
- China
- Prior art keywords
- gear
- positioning
- teeth
- tested
- measuring
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000000034 method Methods 0.000 title claims abstract description 12
- 230000003746 surface roughness Effects 0.000 claims description 25
- 230000005540 biological transmission Effects 0.000 claims description 8
- 230000006978 adaptation Effects 0.000 claims 2
- 238000003780 insertion Methods 0.000 claims 1
- 230000037431 insertion Effects 0.000 claims 1
- 230000000149 penetrating effect Effects 0.000 claims 1
- 238000001514 detection method Methods 0.000 abstract description 13
- 238000009434 installation Methods 0.000 abstract description 2
- 241001422033 Thestylus Species 0.000 description 23
- 238000005259 measurement Methods 0.000 description 21
- 238000010586 diagram Methods 0.000 description 9
- 238000000691 measurement method Methods 0.000 description 6
- 125000006850 spacer group Chemical group 0.000 description 5
- 238000007689 inspection Methods 0.000 description 2
- 238000005070 sampling Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000007812 deficiency Effects 0.000 description 1
- 238000001914 filtration Methods 0.000 description 1
- 239000000523 sample Substances 0.000 description 1
- 238000006467 substitution reaction Methods 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
Images




Classifications
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01M—TESTING STATIC OR DYNAMIC BALANCE OF MACHINES OR STRUCTURES; TESTING OF STRUCTURES OR APPARATUS, NOT OTHERWISE PROVIDED FOR
- G01M13/00—Testing of machine parts
- G01M13/02—Gearings; Transmission mechanisms
- G01M13/021—Gearings
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B21/00—Measuring arrangements or details thereof, where the measuring technique is not covered by the other groups of this subclass, unspecified or not relevant
- G01B21/20—Measuring arrangements or details thereof, where the measuring technique is not covered by the other groups of this subclass, unspecified or not relevant for measuring contours or curvatures, e.g. determining profile
-
- G—PHYSICS
- G01—MEASURING; TESTING
- G01B—MEASURING LENGTH, THICKNESS OR SIMILAR LINEAR DIMENSIONS; MEASURING ANGLES; MEASURING AREAS; MEASURING IRREGULARITIES OF SURFACES OR CONTOURS
- G01B21/00—Measuring arrangements or details thereof, where the measuring technique is not covered by the other groups of this subclass, unspecified or not relevant
- G01B21/30—Measuring arrangements or details thereof, where the measuring technique is not covered by the other groups of this subclass, unspecified or not relevant for measuring roughness or irregularity of surfaces
Landscapes
- Physics & Mathematics (AREA)
- General Physics & Mathematics (AREA)
- A Measuring Device Byusing Mechanical Method (AREA)
Abstract
本发明公开了一种齿轮定位装置、齿轮测量装置及测量方法,涉及机动车齿轮的检测技术领域,解决了如何定位安装齿轮以及如何不用更换定位夹具即可检测奇数轮齿和偶数轮齿的技术问题。包括固定待测齿轮的定位轴,定位轴上设置有找正球;待测齿轮的一侧设置有定位柱;定位柱上安装有锁止销,锁止销上设置有轮齿榫,轮齿榫上设置有轮齿眼。本发明通过定位轴固定待测齿轮的位置,再通过定位柱上的锁止销防止待测齿轮的转动,解决了待测齿轮定位安装的问题。当待测齿轮的轮齿数量为奇数时,通过轮齿榫插入轮齿槽能够锁定待测齿轮;当待测齿轮的轮齿数量为偶数时,通过轮齿眼卡接在轮齿上也能够锁定待测齿轮,从而满足奇数轮齿和偶数轮齿的检测要求。
The invention discloses a gear positioning device, a gear measuring device and a measuring method, relates to the technical field of motor vehicle gear detection, and solves the technology of how to locate and install the gear and how to detect the odd-numbered gear teeth and the even-numbered gear teeth without replacing the positioning fixture question. It includes a positioning shaft for fixing the gear to be tested, and the positioning shaft is provided with an alignment ball; one side of the gear to be tested is provided with a positioning column; Gear teeth are arranged on the tenon. The invention fixes the position of the gear to be tested by the positioning shaft, and then prevents the gear to be tested from rotating through the locking pin on the positioning column, which solves the problem of positioning and installation of the gear to be tested. When the number of teeth of the gear to be tested is an odd number, the gear to be tested can be locked by inserting the tenon of the gear teeth into the tooth slot; Lock the gear to be tested to meet the detection requirements of odd and even teeth.
Description
技术领域technical field
本发明涉及机动车齿轮的检测技术领域,具体来说,是指一种齿轮定位装置、齿轮测量装置及测量方法。The invention relates to the technical field of detection of motor vehicle gears, in particular to a gear positioning device, a gear measuring device and a measuring method.
背景技术Background technique
从电动车的构造上来看,电机的运行效率尤为重要,多档化变速器的设计是保证电机运行效率的重要因素。多档变速器的传动比和换挡策略的相互结合能够大幅提高电动车的电机效率,从而达到高运行、长里程、低损耗、低浪费等诸多优点。From the perspective of the structure of electric vehicles, the operating efficiency of the motor is particularly important, and the design of the multi-speed transmission is an important factor to ensure the operating efficiency of the motor. The combination of the transmission ratio and shifting strategy of the multi-speed transmission can greatly improve the motor efficiency of electric vehicles, thereby achieving many advantages such as high operation, long mileage, low loss, and low waste.
同步器是变速器中复杂关键的部件,齿套和结合齿是同步器中复杂关键的部件,而倒锥和梅角工艺又是齿套的复杂关键的工艺程序。同步器在设计和加工检测方面正不断向更精密的方向发展,齿套梅角的检测精度决定了零件的成品精度。现有技术中,大部分汽车企业通过表面粗糙度轮廓仪或者数显千分表来检测齿套和结合齿的梅角或者倒锥,但齿套或者结合齿的轮齿数量有奇偶之分。对不同轮齿数量的齿轮需要采用不同的定位夹具,而频繁的更换定位夹具导致同步器的检测工作效率较低。此外,对于不同的定位夹具,在检测齿轮的轮齿时,首先需要确定的是测量基准点。但是,现有技术中检测齿轮大多通过人工选择测量基准点的方式进行检测,导致检测结果的误差偏大,不利于提高齿轮的检测精度。Synchronizer is a complex and key part in transmission, gear sleeve and combined tooth are complex and key parts in synchronizer, and reverse taper and plum angle process are complex and key process procedures of gear sleeve. Synchronizers are constantly developing in a more precise direction in terms of design and processing inspection. The inspection accuracy of the plume angle of the gear sleeve determines the finished product accuracy of the parts. In the prior art, most automobile companies use a surface roughness profiler or a digital dial indicator to detect the plume angle or reverse taper of the tooth sleeve and the combined tooth, but the number of gear teeth of the tooth sleeve or the combined tooth is divided into odd and even. Different positioning fixtures need to be used for gears with different numbers of teeth, and frequent replacement of positioning fixtures leads to lower detection efficiency of the synchronizer. In addition, for different positioning fixtures, the first thing that needs to be determined is the measurement reference point when detecting the teeth of the gear. However, most of the detection gears in the prior art are detected by manually selecting measurement reference points, which leads to a large error in the detection results, which is not conducive to improving the detection accuracy of the gears.
发明内容SUMMARY OF THE INVENTION
有鉴于此,本发明的目的在于克服现有技术的不足,第一方面,提供一种齿轮定位装置,以解决如何定位安装齿轮以及如何不用更换定位夹具即可检测奇数轮齿和偶数轮齿的技术问题。In view of this, the purpose of the present invention is to overcome the deficiencies of the prior art. In the first aspect, a gear positioning device is provided to solve how to position and install the gear and how to detect the odd-numbered gear teeth and the even-numbered gear teeth without changing the positioning fixture. technical problem.
本发明解决该技术问题所采用的技术方案是:The technical scheme adopted by the present invention to solve the technical problem is:
一种齿轮定位装置,用于定位待测齿轮,包括:A gear positioning device for positioning the gear to be tested, comprising:
定位轴,所述待测齿轮外套于所述定位轴上,所述定位轴的顶部设置有用于确定测量中心的找正球;a positioning shaft, the gear to be measured is sleeved on the positioning shaft, and the top of the positioning shaft is provided with an alignment ball for determining the measurement center;
定位柱,设置于所述待测齿轮的一侧;以及,a positioning column, arranged on one side of the gear to be tested; and,
锁止销,安装在所述定位柱上,所述锁止销位于所述待测齿轮的轮齿一侧;a locking pin, mounted on the positioning column, and the locking pin is located on one side of the gear teeth of the gear to be tested;
其中,所述锁止销上设置有与所述待测齿轮的轮齿槽相适配的轮齿榫,所述轮齿榫上设置有与所述待测齿轮的轮齿相适配的轮齿眼,使所述锁止销选择性的插入所述轮齿槽内,或者,卡接在所述轮齿上。Wherein, the locking pin is provided with a tooth tenon which is adapted to the tooth groove of the gear to be tested, and the gear tenon is provided with a wheel which is adapted to the tooth of the gear to be tested. A tooth eye, so that the locking pin is selectively inserted into the gear tooth slot, or is clamped on the gear tooth.
在上述技术方案的基础上,该齿轮定位装置还可以做如下的改进。On the basis of the above technical solutions, the gear positioning device can also be improved as follows.
可选的,所述定位柱上设置有锁止槽,所述锁止销安装在所述锁止槽内,在所述定位柱与所述锁止销之间安装有弹性件,所述弹性件将所述锁止销顶推在所述轮齿槽内或者轮齿上。Optionally, the positioning column is provided with a locking groove, the locking pin is installed in the locking groove, an elastic member is installed between the positioning column and the locking pin, and the elastic A piece pushes the locking pin into the gear tooth slot or on the gear tooth.
可选的,所述锁止销的尾部设置有限位件,所述锁止销贯穿所述定位柱后通过所述限位件限位安装在所述锁止槽内。Optionally, a stopper is provided at the tail of the locking pin, and the locking pin is installed in the locking groove through the stopper after passing through the positioning column.
可选的,所述定位轴外套有与所述待测齿轮的内径相适配的衬套,所述衬套外套有垫片,所述垫片使所述待测齿轮的轮齿位于所述锁止销的位置。Optionally, the positioning shaft is covered with a bushing that matches the inner diameter of the gear to be measured, and the bushing is covered with a spacer, and the spacer makes the gear teeth of the gear to be measured located in the position of the locking pin.
可选的,所述定位轴还外套有压片,所述压片沿所述定位轴的轴向将所述待测齿轮压紧在所述垫片上。Optionally, the positioning shaft is also covered with a pressing sheet, and the pressing sheet presses the gear to be measured on the gasket along the axial direction of the positioning shaft.
可选的,所述定位轴与所述定位柱均连接有底座,所述底座还设置有用于与表面粗糙度轮廓仪的工作台连接的连接孔。Optionally, both the positioning shaft and the positioning column are connected with a base, and the base is further provided with a connection hole for connecting with a workbench of the surface roughness profiler.
第二方面,本发明还提供一种齿轮测量装置,包括表面粗糙度轮廓仪以及上述的齿轮定位装置,所述齿轮定位装置安装在所述表面粗糙度轮廓仪的工作台上,所述表面粗糙度轮廓仪上的测针对所述待测齿轮进行测量。In a second aspect, the present invention also provides a gear measuring device, comprising a surface roughness profiler and the above-mentioned gear positioning device, wherein the gear positioning device is installed on a workbench of the surface roughness profiler, and the surface roughness The probe on the profilometer measures the gear to be tested.
第三方面,本发明还提供一种齿轮测量方法,使用上述的齿轮测量装置,包括以下步骤:In a third aspect, the present invention also provides a gear measurement method, using the above-mentioned gear measurement device, comprising the following steps:
S1、确定所述表面粗糙度轮廓仪的工作台传输的方向为Y向,确定所述定位轴的轴向为Z向,确定与所述Y向以及Z向分别垂直的方向为X向;S1. Determine that the transmission direction of the table of the surface roughness profiler is the Y direction, determine that the axial direction of the positioning axis is the Z direction, and determine that the directions perpendicular to the Y direction and the Z direction are the X direction;
S2、将所述待测齿轮固定在所述定位轴上,通过所述锁止销锁定所述待测齿轮,将所述齿轮定位装置固定在所述工作台上;S2. Fix the gear to be measured on the positioning shaft, lock the gear to be measured through the locking pin, and fix the gear positioning device on the worktable;
S3、通过所述表面粗糙度轮廓仪的测针确定所述找正球的球心在所述Z向上延长线的位置;S3. Determine the position of the center of the alignment sphere on the Z-direction extension line through the stylus of the surface roughness profiler;
S4、所述待测齿轮随所述工作台沿所述Y向移动,当所述待测齿轮的轮齿移动至所述测针位置时,所述测针在所述X向和Z向上移动以测量所述待测齿轮的轮廓曲线。S4. The gear to be tested moves along the Y direction with the worktable. When the gear teeth of the gear to be tested move to the position of the stylus, the stylus moves in the X and Z directions. to measure the profile curve of the gear to be tested.
在上述技术方案的基础上,该齿轮测量方法还可以做如下的改进。On the basis of the above technical solutions, the gear measurement method can also be improved as follows.
可选的,所述步骤S3包括以下步骤:Optionally, the step S3 includes the following steps:
S31、所述测针沿所述X向在所述找正球上任意拉取三条曲线;S31, the stylus arbitrarily pulls three curves along the X direction on the alignment ball;
S32、通过所述测针测得所述三条曲线的最高点分别为A、B、C;S32, the highest points of the three curves measured by the stylus are A, B, and C respectively;
S33、通过所述A、B、C三点确定位于所述找正球上的一个圆形截面,所述圆形截面与所述找正球的相交线为曲线S;S33, determine a circular section located on the alignment sphere through the three points A, B, and C, and the intersection line of the circular section and the alignment sphere is a curve S;
S34、通过所述测针测得所述曲线S的最高点。S34. Measure the highest point of the curve S through the stylus.
可选的,所述步骤S2中:Optionally, in the step S2:
当所述待测齿轮的轮齿数量为奇数时,转动所述锁止销,通过所述轮齿榫插入所述待测齿轮的轮齿槽内;或者,When the number of teeth of the gear to be tested is an odd number, the locking pin is rotated and inserted into the tooth groove of the gear to be tested through the tooth tenon; or,
当所述待测齿轮的轮齿数量为偶数时,转动所述锁止销,通过所述轮齿眼卡接在所述待测齿轮的轮齿上。When the number of teeth of the gear to be tested is an even number, the locking pin is rotated to be clamped on the teeth of the gear to be tested through the tooth eye.
与现有技术相比,本发明提供的齿轮定位装置具有的有益效果是:Compared with the prior art, the gear positioning device provided by the present invention has the following beneficial effects:
1、本发明通过定位轴固定待测齿轮的位置,再通过定位柱上的锁止销防止待测齿轮的转动,解决了待测齿轮定位安装的问题。当待测齿轮的轮齿数量为奇数时,通过轮齿榫插入轮齿槽能够锁定待测齿轮;当待测齿轮的轮齿数量为偶数时,通过轮齿眼卡接在轮齿上同样能够锁定待测齿轮,从而满足奇数轮齿和偶数轮齿的检测要求。同时,本发明的锁止销能够旋转任意的角度适应不同倾斜角度的轮齿,不仅使用范围广,而且操作简单方便,能够提高同步器检测的工作效率;1. The present invention fixes the position of the gear to be measured through the positioning shaft, and then prevents the rotation of the gear to be measured through the locking pin on the positioning column, which solves the problem of positioning and installation of the gear to be measured. When the number of teeth of the gear to be tested is an odd number, the gear to be tested can be locked by inserting the tenon of the gear teeth into the tooth slot; when the number of teeth of the gear to be tested is an even number, it can be also Lock the gear to be tested to meet the detection requirements of odd and even teeth. At the same time, the locking pin of the present invention can rotate at any angle to adapt to the gear teeth of different inclination angles, not only has a wide range of use, but also is simple and convenient to operate, and can improve the work efficiency of the synchronizer detection;
2、本发明通过测针确定找正球的球心位置,再利用球心在Z向上的延长线作为齿轮轮齿检测的测量基准线,通过检测轮齿各结构面相对于球心的坐标,能够检测出齿套和结合齿的倒锥或者梅角参数,避免了人工选择测量基准点的检测步骤,提高了齿轮检测的精度。同时,配合计算机控制表面粗糙度轮廓仪的动作,还能够实现待测齿轮的自动定位与自动测量。2. In the present invention, the position of the center of the alignment ball is determined by the stylus, and the extension line of the center of the ball in the Z direction is used as the measurement reference line for the detection of the gear teeth. The inverted cone or plum angle parameters of the tooth sleeve and the combined tooth are detected, which avoids the detection step of manually selecting the measurement reference point, and improves the accuracy of gear detection. At the same time, with the action of the surface roughness profiler controlled by the computer, the automatic positioning and automatic measurement of the gear to be measured can also be realized.
附图说明Description of drawings
为了更清楚地说明本发明实施例或现有技术中的技术方案,下面将对实施例或现有技术描述中所需要使用的附图作简单地介绍,显而易见地,下面描述中的附图仅仅是本发明的一些实施例,对于本领域普通技术人员来讲,在不付出创造性劳动的前提下,还可以根据这些附图获得其他的附图。In order to explain the embodiments of the present invention or the technical solutions in the prior art more clearly, the following briefly introduces the accompanying drawings that need to be used in the description of the embodiments or the prior art. Obviously, the accompanying drawings in the following description are only These are some embodiments of the present invention. For those of ordinary skill in the art, other drawings can also be obtained according to these drawings without creative efforts.
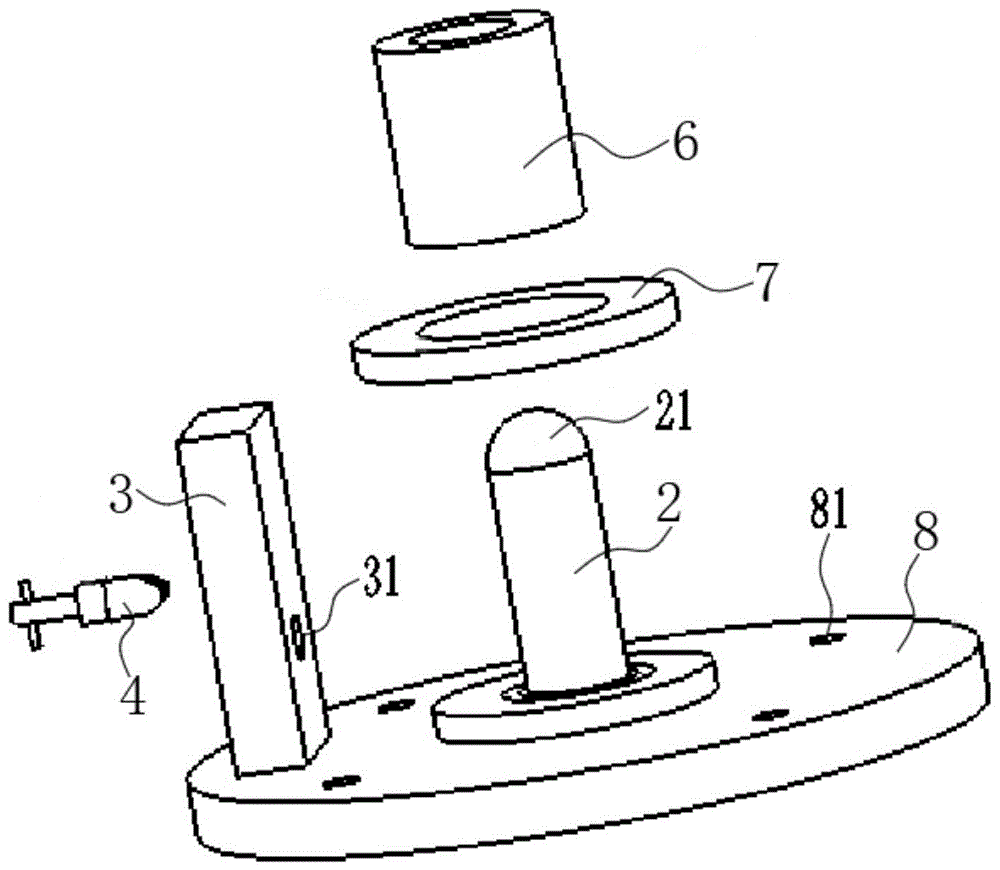
图1是本发明齿轮定位装置的分解结构示意图;Fig. 1 is the exploded structure schematic diagram of the gear positioning device of the present invention;
图2是本发明齿轮定位装置的组合结构示意图;Fig. 2 is the combined structure schematic diagram of the gear positioning device of the present invention;
图3是本发明齿轮测量装置测量待测齿轮的结构示意图;3 is a schematic structural diagram of the gear measuring device of the present invention measuring the gear to be measured;
图4是本发明齿轮测量装置测量待测齿轮的另一结构示意图;Fig. 4 is another structural schematic diagram of the gear measuring device of the present invention measuring the gear to be measured;
图5是本发明齿轮测量装置测量待测齿轮的又一结构示意图;Fig. 5 is another structural schematic diagram of the gear measuring device of the present invention measuring the gear to be measured;
图6是图1中锁止销的立体结构示意图;Fig. 6 is the three-dimensional structure schematic diagram of the locking pin in Fig. 1;
图7是图3中锁止销与待测齿轮锁定的结构示意图;FIG. 7 is a schematic structural diagram of locking the locking pin and the gear to be tested in FIG. 3;
图8是测针在找正球上任意拉取三条曲线的结构示意图;Figure 8 is a schematic diagram of the structure of the stylus pulling three curves arbitrarily on the setting ball;
图9是通过三个最高点确定测量中心的结构示意图;Fig. 9 is the structural schematic diagram of determining the measurement center by three highest points;
图10是本发明齿轮测量方法的流程图。Fig. 10 is a flow chart of the gear measurement method of the present invention.
图中:In the picture:
1—待测齿轮;2—定位轴;21—找正球;3—定位柱;31—锁止槽;4—锁止销;41—轮齿榫;42—轮齿眼;43—限位件;5—弹性件;6—衬套;7—垫片;8—底座;81—连接孔;9—测针。1—gear to be tested; 2—positioning shaft; 21—aligning ball; 3—positioning column; 31—locking groove; 4—locking pin; 41—gear tenon; 42—gear tooth eye; 43—limiting
具体实施方式Detailed ways
为使本发明的目的、技术方案和优点更加清楚,下面将对本发明的技术方案进行详细的描述。显然,所描述的实施例仅仅是本发明一部分实施例,而不是全面的实施例。基于本发明中的实施例,本领域普通技术人员在没有做出创造性劳动的前提下所得到的所有其它实施方式,都属于本发明所保护的范围。In order to make the objectives, technical solutions and advantages of the present invention clearer, the technical solutions of the present invention will be described in detail below. Obviously, the described embodiments are only some of the embodiments of the present invention, and not all of them. Based on the embodiments of the present invention, all other implementations obtained by those of ordinary skill in the art without creative work fall within the protection scope of the present invention.
实施例1:Example 1:
本发明提供一种齿轮定位装置,如图1至图7所示,包括定位轴2、定位柱3以及锁止销4。待测齿轮1的轴孔套接在定位轴2上,使待测齿轮1固定在平面上。根据待测齿轮1轴孔的尺寸,可以选择尺寸适配的衬套6套接在定位轴2上,使待测齿轮1稳固的固定。在定位轴2的顶部设置有半球形结构的找正球21,找正球21的球心位于定位轴2的轴线上,方便确定待测齿了1的测量中心。The present invention provides a gear positioning device, as shown in FIG. 1 to FIG. 7 , comprising a
如图1至图7所示,定位柱3设置在待测齿轮1的一侧,定位柱3上设置有锁止槽31,锁止销4安装在锁止槽31内。如图6所示,特别地,锁止销4的头部为楔形结构的轮齿榫41,轮齿榫41能够插入待测齿轮1的轮齿槽内。同时,在轮齿榫41上开设有V字形的轮齿眼42,轮齿眼42能够卡接在待测齿轮1的轮齿上。As shown in FIG. 1 to FIG. 7 , the
当待测齿轮1的轮齿数量为奇数时,则通过轮齿榫41插入轮齿槽能够锁定待测齿轮1。当待测齿轮1的轮齿数量为偶数时,则转动锁止销4,通过轮齿眼42卡接在轮齿上同样能够锁定待测齿轮1,保证了待测齿轮1在锁止销4的延伸方向上是轮齿而不是轮齿槽,从而方便待测齿轮1的测量。When the number of teeth of the gear to be tested 1 is odd, the gear to be tested 1 can be locked by inserting the
本发明的锁止销4设计既可以满足奇数轮齿的测量,又可以满足偶数轮齿的测量。同时,当待测齿轮1的轮齿为螺旋齿时,本发明的锁止销4能够通过旋转任意角度以适应不同倾斜角度的轮齿固定,并且同样适用于奇数轮齿或者偶数轮齿的螺旋齿。The design of the
如图7所示,在定位柱3与锁止销4之间安装有弹性件5,弹性件5可以选用弹簧、碟簧或者弹片等结构,使锁止销4在弹性件5的弹性作用下顶推在待测齿轮1的轮齿槽内或者轮齿上。在锁止销4的尾部设置有限位件43,限位件43可以是挡杆或者挡板等结构,锁止销4贯穿定位柱3后通过限位件43限位安装在锁止槽31内。当然,根据锁止销4不同的结构形式,锁止槽31既可以设计为盲孔的结构形式,也可以设计为通孔的结构形式。As shown in FIG. 7 , an
如图1至图5所示,衬套6还外套有垫片7,待测齿轮1套接在定位轴2后位于垫片7的上方。垫片7能够使待测齿轮1的轮齿位于锁止销4延长线的位置,从而使锁止销4顶推待测齿轮1的轮齿部位。特别地,在待测齿轮1的顶部还设置有压片(图中未示出),压片过渡连接在定位轴2上,使待测齿轮1能够沿定位轴2的轴向压紧在垫片7上。当然,根据不同齿轮的不同厚度,可以选择更多数量的垫片7。As shown in FIG. 1 to FIG. 5 , the
如图1至图5所示,在定位轴2与定位柱3的底部设置有底座8,底座8为圆盘型结构。定位轴2位于底座8的中心,定位柱3位于底座8的边缘。在底座8上还开设有连接孔81,使齿轮定位装置能够通过螺栓贯穿连接孔81后安装在表面粗糙度轮廓仪的工作台上。当然,定位轴2与定位柱3也可以分别连接在表面粗糙度轮廓仪的工作台上。As shown in FIG. 1 to FIG. 5 , a
可以理解的是,根据齿轮的不同规格,通过选择不同尺寸、数量的衬套6以及垫片7,能够在同一个齿轮定位装置中安装不同规格的待测齿轮1。本发明通过这种结构设计,能够对不同齿数、不同倾斜角度的轮齿以及不同尺寸的待测齿轮1进行定位安装,不仅使用范围广,而且操作简单方便。It can be understood that, according to different specifications of the gears, by selecting different sizes and quantities of
实施例2:Example 2:
本发明还提供一种齿轮测量装置,如图3至图5所示,包括表面粗糙度轮廓仪以及上述的齿轮定位装置。表面粗糙度轮廓仪上设置有工作台以及测针9。齿轮定位装置通过底座8上的连接孔81安装在工作台上,表面粗糙度轮廓仪上的测针9对待测齿轮1进行测量。The present invention also provides a gear measuring device, as shown in FIGS. 3 to 5 , comprising a surface roughness profiler and the above-mentioned gear positioning device. A table and a
测针9与待测齿轮1的轮齿接触,并且将接触信息传递至表面粗糙度轮廓仪主机上的传感零件。在测量过程中,测针9相对待测齿轮1轮齿的表面作匀速滑行,以感受被测表面的几何变化。表面粗糙度轮廓仪主机将测针9采样的信息转换成电信号,该电信号经放大和处理转换成数字信号储存在计算机系统的存储器中。The
计算机系统对待测齿轮1的表面信息进行数字滤波,分离掉待测齿轮1的表面粗糙度成分后再进行计算。测量结果为计算出的符合某种曲线的实际值以及离测量中心的坐标值,或者是放大的实际轮廓曲线。最终测量结果通过显示器或者打印机输出。一般情况下,测针9是沿定位轴2的轴向以及工作台移动方向的垂直方向移动采样。The computer system performs digital filtering on the surface information of the
实施例3:Example 3:
本发明还提供一种齿轮测量方法,如图1至图10所示,使用上述的齿轮测量装置。首先,确定表面粗糙度轮廓仪的工作台传输的方向为Y向,确定定位轴2的轴向为Z向,确定与Y向以及Z向分别垂直的方向为X向,即建立关于XYZ的三维空间坐标系。The present invention also provides a gear measurement method, as shown in FIGS. 1 to 10 , using the above-mentioned gear measurement device. First, determine the transmission direction of the worktable of the surface roughness profiler as the Y direction, determine the axial direction of the
然后,将待测齿轮1定位安装在定位轴2上。此时,可以根据待测齿轮1的规格选择数量以及尺寸适配的衬套6、垫片7以及压片来固定待测齿轮1。当待测齿轮1的轮齿数量为奇数时,转动锁止销4,通过轮齿榫41插入待测齿轮1的轮齿槽内以锁定待测齿轮1。或者,当待测齿轮1的轮齿数量为偶数时,转动锁止销4,通过轮齿眼42卡接在待测齿轮1的轮齿上以锁定待测齿轮1。再通过连接孔81将齿轮定位装置固定在工作台上,并且使锁止销4的延长线方向与工作台的传输方向相同。Then, the
如图8与图9所示,重要的是,通过表面粗糙度轮廓仪的测针9确定找正球21的球心在Z向上延长线的位置,找正球21的球心即XYZ三维空间坐标系的原点。具体来说,将测针9沿X向在找正球21上任意拉取三条曲线。由于测针9是沿X向和Z向移动的,相当于用平行于XZ平面的三个平面去截取找正球21。三个平面分别与找正球21的表面相交形成三条曲线,通过测针9能够测得三条曲线的最高点分别为A、B、C,即A、B、C三点分别为三条曲线中Z向值最大的点。As shown in FIGS. 8 and 9 , it is important to determine the position of the center of the
此时,由于找正球21为半球形结构,找正球21表面各点与球心之间的距离均相同。不难发现,A、B、C三点的X向坐标距离相等,并且A、B、C三点所在的平面为YZ平面。利用三点确定一个圆的原理,则通过A、B、C三点能够确定出位于找正球21上的一个圆形截面。该圆形截面与找正球21的相交线为曲线S,通过测针9能够测得曲线S的最高点。则球心与曲线S最高点之间的连线即为球心在Z向上的延长线,以此延长线作为测量中心线。重复以上步骤,能够提高测量中心线定位的精度。At this time, since the
最后,待测齿轮1随工作台沿Y向移动,当待测齿轮1的轮齿移动至测针9位置时,测针9在X向和Z向上移动采样,能够测得待测齿轮1的轮廓曲线。测量结果在计算机系统中自动放大为实际轮廓曲线,通过计算该曲线的夹角就能够得出待测齿轮1的梅角夹角的大小。同样的方法,还可以测量待测齿轮1的倒锥夹角的大小。Finally, the
本发明的齿轮测量方法,通过在找正球21上任意选择三条曲线,通过三条曲线的三个最高点确定圆形截面,并且以圆形截面的最高点作为测量中心线。避免了人工选择基准测量点的步骤,从而避免了人工选择导致的精度低的问题。本发明仅需要将待测齿轮1安装在齿轮定位装置上,点击计算机上的开始测量按钮,即可使测针9自动确定测量中心线,并且测量中心线的选择精度高,自动化程度高。不仅可以实现完全自动化的测量过程,而且能够提高同步器齿套以及结合齿的检测精度,降低换档卡滞,提高换档的平顺性。In the gear measurement method of the present invention, three curves are arbitrarily selected on the setting
可以理解的是,本发明的齿轮测量方法还可以通过表面粗糙度轮廓仪的工作台带动找正球21沿Y向移动,使测针9相对于找正球21沿Y向在找正球21上任意拉取三条曲线。然后通过测针9测得三条曲线的最高点,三个最高点能够确定XZ平面内的圆形截面,通过测针9测得该圆形截面的最高点,同样能够确定球心在Z向上的延长线。It can be understood that, the gear measurement method of the present invention can also drive the
以上所述,仅为本发明的具体实施方式,但本发明的保护范围并不局限于此,任何熟悉本技术领域的技术人员在本发明揭露的技术范围内,可轻易想到变化或替换,都应涵盖在本发明的保护范围之内。The above are only specific embodiments of the present invention, but the protection scope of the present invention is not limited to this. Any person skilled in the art can easily think of changes or substitutions within the technical scope disclosed by the present invention. should be included within the protection scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010867617.9A CN112051054B (en) | 2020-08-26 | 2020-08-26 | Gear positioning device, gear measuring device and measuring method |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202010867617.9A CN112051054B (en) | 2020-08-26 | 2020-08-26 | Gear positioning device, gear measuring device and measuring method |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN112051054A true CN112051054A (en) | 2020-12-08 |
| CN112051054B CN112051054B (en) | 2021-12-07 |
Family
ID=73599911
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202010867617.9A Active CN112051054B (en) | 2020-08-26 | 2020-08-26 | Gear positioning device, gear measuring device and measuring method |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN112051054B (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112857981A (en) * | 2020-12-28 | 2021-05-28 | 国营第六一六厂 | Clamp for testing strength of gear teeth of cylindrical straight-tooth gear |
| CN115265321A (en) * | 2022-07-11 | 2022-11-01 | 东风汽车股份有限公司 | Device for detecting inclination of conical surface of valve seat of cylinder cover and using method of device |
| CN115854812A (en) * | 2022-11-22 | 2023-03-28 | 东风本田发动机有限公司 | Detection device and detection method |
| CN116222484A (en) * | 2023-03-14 | 2023-06-06 | 南京南传智能技术有限公司 | Angular error measuring device for internal and external teeth of planetary gear |
| WO2023230772A1 (en) * | 2022-05-30 | 2023-12-07 | 玉环普天单向器有限公司 | Measurement device and method for straightness of planetary gear finished product |
Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2224396Y (en) * | 1994-08-26 | 1996-04-10 | 刘曙军 | Involute cylindrical-gear divided-arc thooth thick measuring device |
| JP2002310643A (en) * | 2001-04-12 | 2002-10-23 | Isuzu Motors Ltd | Gear angle measuring method and gear angle inspection device |
| CN2655176Y (en) * | 2003-06-06 | 2004-11-10 | 上海凯力博电器仪表成套有限公司 | Roughness contour meter |
| CN101655163A (en) * | 2009-09-17 | 2010-02-24 | 上海汽车变速器有限公司 | Fixed stroke synchronizer |
| CN206321183U (en) * | 2016-12-14 | 2017-07-11 | 江门市力泰科技有限公司 | A kind of synchronous gear sleeve plum angle depth check tool |
| CN207423138U (en) * | 2017-11-13 | 2018-05-29 | 东风格特拉克汽车变速箱有限公司 | A kind of gear chamfering detects fixture |
| CN209783898U (en) * | 2019-05-16 | 2019-12-13 | 重庆诚扬精密制造有限公司 | gear detector |
| CN111060309A (en) * | 2020-01-17 | 2020-04-24 | 瑞斯恩智能科技(苏州)有限公司 | Gear detection machine and detection method |
| CN210603898U (en) * | 2019-09-09 | 2020-05-22 | 事必达(肇庆)精密制造有限公司 | Multifunctional gear measuring instrument |
| CN210664389U (en) * | 2019-10-23 | 2020-06-02 | 晟邦精密工业(苏州)有限公司 | Gear detection device |
-
2020
- 2020-08-26 CN CN202010867617.9A patent/CN112051054B/en active Active
Patent Citations (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN2224396Y (en) * | 1994-08-26 | 1996-04-10 | 刘曙军 | Involute cylindrical-gear divided-arc thooth thick measuring device |
| JP2002310643A (en) * | 2001-04-12 | 2002-10-23 | Isuzu Motors Ltd | Gear angle measuring method and gear angle inspection device |
| CN2655176Y (en) * | 2003-06-06 | 2004-11-10 | 上海凯力博电器仪表成套有限公司 | Roughness contour meter |
| CN101655163A (en) * | 2009-09-17 | 2010-02-24 | 上海汽车变速器有限公司 | Fixed stroke synchronizer |
| CN206321183U (en) * | 2016-12-14 | 2017-07-11 | 江门市力泰科技有限公司 | A kind of synchronous gear sleeve plum angle depth check tool |
| CN207423138U (en) * | 2017-11-13 | 2018-05-29 | 东风格特拉克汽车变速箱有限公司 | A kind of gear chamfering detects fixture |
| CN209783898U (en) * | 2019-05-16 | 2019-12-13 | 重庆诚扬精密制造有限公司 | gear detector |
| CN210603898U (en) * | 2019-09-09 | 2020-05-22 | 事必达(肇庆)精密制造有限公司 | Multifunctional gear measuring instrument |
| CN210664389U (en) * | 2019-10-23 | 2020-06-02 | 晟邦精密工业(苏州)有限公司 | Gear detection device |
| CN111060309A (en) * | 2020-01-17 | 2020-04-24 | 瑞斯恩智能科技(苏州)有限公司 | Gear detection machine and detection method |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112857981A (en) * | 2020-12-28 | 2021-05-28 | 国营第六一六厂 | Clamp for testing strength of gear teeth of cylindrical straight-tooth gear |
| WO2023230772A1 (en) * | 2022-05-30 | 2023-12-07 | 玉环普天单向器有限公司 | Measurement device and method for straightness of planetary gear finished product |
| CN115265321A (en) * | 2022-07-11 | 2022-11-01 | 东风汽车股份有限公司 | Device for detecting inclination of conical surface of valve seat of cylinder cover and using method of device |
| CN115854812A (en) * | 2022-11-22 | 2023-03-28 | 东风本田发动机有限公司 | Detection device and detection method |
| CN116222484A (en) * | 2023-03-14 | 2023-06-06 | 南京南传智能技术有限公司 | Angular error measuring device for internal and external teeth of planetary gear |
Also Published As
| Publication number | Publication date |
|---|---|
| CN112051054B (en) | 2021-12-07 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN112051054B (en) | Gear positioning device, gear measuring device and measuring method | |
| CN102607433B (en) | Multi-point detection device for thickness of bearing bush | |
| CN110207565A (en) | A kind of high speed warp knit machine crankshaft rigging position degree measurement tooling and measurement method | |
| WO2015089689A1 (en) | Micrometer for inner and outer diameter detection | |
| CN204165479U (en) | Deep hole diameter run-out cubing in axle | |
| CN2835944Y (en) | Measuring tool for measuring coaxial relative position | |
| CN211147543U (en) | Gauge for measuring groove depth of gear sleeve locking block | |
| CN214121126U (en) | Detection tool for detecting diameter and roundness of spherical surface | |
| CN210981108U (en) | Internal spline tooth top circle diameter inspection fixture | |
| CN220818784U (en) | CVT driving shaft conical surface measuring point position gauge | |
| CN204988228U (en) | Screw rod detection device | |
| CN110849246A (en) | Device and method for rapidly detecting size of inner arc of magnetic shoe | |
| CN216745891U (en) | Connecting rod cover bolt connecting hole end face verticality detection device | |
| CN116222484B (en) | Planetary gear internal and external tooth angle error measuring device | |
| CN216954346U (en) | Extension rod assembly angle detection clamp of steering machine | |
| CN215491403U (en) | Slip teeth of a cogwheel is beated and is measured anchor clamps | |
| CN113188423B (en) | Positioning device and system for detecting symmetry degree of radial hole of shaft part | |
| CN205245979U (en) | Hole groove axiality detector | |
| CN116734707A (en) | Measuring synchronizer combined tooth edge line angle gauge | |
| CN203479229U (en) | Gauge used for detecting distance between spherical surface and axis | |
| CN210400236U (en) | Detection tool for detecting height and parallelism of rib of inner ring of tapered roller bearing | |
| CN108592730B (en) | A kind of micrometer caliper | |
| CN108955492B (en) | Method and device for measuring machining residue of straight tooth chamfer of shaft tooth part | |
| CN201110748Y (en) | Bore circular arc and pyramidal face intersecting line position dimension measuring device | |
| CN204007453U (en) | Oil pipes internal thread pitchometer |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PB01 | Publication | ||
| PB01 | Publication | ||
| SE01 | Entry into force of request for substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| GR01 | Patent grant | ||
| GR01 | Patent grant |