CN103406603A - Elastic locating and locking device for milled teeth of bevel gear shaft - Google Patents
Elastic locating and locking device for milled teeth of bevel gear shaft Download PDFInfo
- Publication number
- CN103406603A CN103406603A CN2013102020999A CN201310202099A CN103406603A CN 103406603 A CN103406603 A CN 103406603A CN 2013102020999 A CN2013102020999 A CN 2013102020999A CN 201310202099 A CN201310202099 A CN 201310202099A CN 103406603 A CN103406603 A CN 103406603A
- Authority
- CN
- China
- Prior art keywords
- sleeve
- spring sleeve
- milling
- positioning
- locking spring
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Pending
Links
Images

Landscapes
- Gear Processing (AREA)
Abstract
本发明涉及锥齿轮轴加工技术领域,具体地说是一种锥齿轮轴铣齿弹性定位锁紧装置。传统的加工是将工件直接装在铣齿胎里,然后用拉杆将工件拉紧后进行加工,这种装夹方式使工件与铣齿胎配合间隙无法保证,致使产品加工质量差。本发明由铣齿胎体、套筒、锁紧弹簧套、丝堵和定位弹簧套组成。铣齿胎体右端与套筒左半部为螺纹配合联接在一起;带开口槽的锁紧弹簧套放入套筒内,锁紧弹簧套与套筒前后各有一段设为间隙配合接触,套筒左端与锁紧弹簧套左端锥面配合,且锁紧弹簧套左端外锥面可沿套筒左端内锥面轴向移动;丝堵一端与锁紧弹簧套为螺纹配合联接在一起;铣齿胎体前端装有带开口槽的定位弹簧套。本发明定位精度高、操作简单、使用方便。
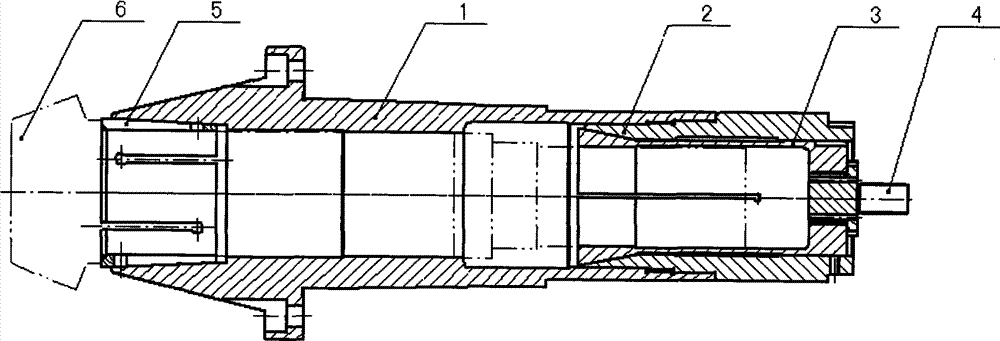
The invention relates to the technical field of bevel gear shaft processing, in particular to an elastic positioning and locking device for milling teeth of a bevel gear shaft. The traditional processing is to directly install the workpiece in the milling tire, and then use the tie rod to tighten the workpiece before processing. This clamping method makes the gap between the workpiece and the milling tire impossible to guarantee, resulting in poor processing quality. The invention is composed of a milling carcass, a sleeve, a locking spring sleeve, a plug and a positioning spring sleeve. The right end of the milling carcass and the left half of the sleeve are threaded and connected together; the locking spring sleeve with an open groove is put into the sleeve, and the locking spring sleeve and the front and rear sections of the sleeve are set as clearance fit contacts. The left end of the barrel cooperates with the taper surface of the left end of the locking spring sleeve, and the outer taper surface of the left end of the locking spring sleeve can move axially along the inner taper surface of the left end of the sleeve; one end of the plug and the locking spring sleeve are threaded and connected together; the teeth are milled The front end of the carcass is equipped with a positioning spring sleeve with an open groove. The invention has high positioning precision, simple operation and convenient use.
Description
技术领域technical field
本发明涉及锥齿轮轴加工技术领域,具体地说是一种锥齿轮轴铣齿弹性定位锁紧装置。The invention relates to the technical field of bevel gear shaft processing, in particular to an elastic positioning and locking device for milling teeth of a bevel gear shaft.
背景技术Background technique
目前,在现有技术中,锥齿轮轴的铣齿加工,采用传统的加工方法比较多,传统的加工方法是采用工件直接装入铣齿胎中,然后用拉杆将工件拉紧后进行加工,工件与铣齿胎是间隙配合,由于间隙配合存在的弊病,配合间隙大零件加工精度保证不了,配合间隙小工件不好装卸。所以此加工方法已远远满足不了现在的高质量产品设计要求,加工精度差、生产效率地,而且操作不方便。At present, in the existing technology, the milling of bevel gear shafts adopts traditional processing methods. The traditional processing method is to directly load the workpiece into the milling tire, and then use the pull rod to tighten the workpiece before processing. The workpiece and the milling tire have a clearance fit. Due to the disadvantages of the clearance fit, the machining accuracy of parts with a large fit clearance cannot be guaranteed, and the workpiece with a small fit clearance is not easy to load and unload. Therefore, this processing method is far from meeting the current high-quality product design requirements, with poor processing accuracy, low production efficiency, and inconvenient operation.
发明内容Contents of the invention
为了解决上述存在的问题,本发明提供了一种产品定位精度高,操作简单、使用方便的锥齿轮轴铣齿弹性定位夹紧装置。In order to solve the above existing problems, the present invention provides a bevel gear shaft milling teeth elastic positioning and clamping device with high product positioning accuracy, simple operation and convenient use.
本发明解决其技术问题所采用的技术方案是:锥齿轮轴铣齿弹性定位锁紧装置由铣齿胎体1、套筒2、锁紧弹簧套3、丝堵4、定位弹簧套5组成。铣齿胎体1右端与套筒2左半部为螺纹配合联接在一起;带开口槽的锁紧弹簧套3放入套筒2内,锁紧弹簧套3与套筒2前后各有一段设为间隙配合接触,套筒2左端与锁紧弹簧套3左端锥面配合,且锁紧弹簧套3左端外锥面可沿套筒2左端内锥面轴向移动;丝堵4一端与锁紧弹簧套3为螺纹配合联接在一起;铣齿胎体1前端装有带开口槽的定位弹簧套5,铣齿胎体1前端内孔锥度与定位弹簧套5外圆锥度一致,采用配磨加工;锥齿轮轴6装入铣齿胎体1内孔中,铣齿胎体1用螺栓固定在机床主轴端面上;丝堵4另一端与机床油压系统联接。The technical solution adopted by the present invention to solve the technical problem is: the bevel gear shaft milling elastic positioning locking device is composed of a milling carcass 1, a sleeve 2, a
本发明的有益效果是,由于定位弹簧套不会与工件产生摩擦,所以装卸方便。并且定位精度高,操作简单、使用方便,该装置可快速实现工件的定位装夹及加工。尤其适用批量生产。The beneficial effect of the invention is that, since the positioning spring sleeve does not generate friction with the workpiece, it is convenient to assemble and disassemble. Moreover, the positioning accuracy is high, the operation is simple, and the use is convenient. The device can quickly realize the positioning, clamping and processing of the workpiece. Especially suitable for mass production.
附图说明Description of drawings
图1是本发明锥齿轮轴铣齿弹性定位锁紧装置的结构图。Fig. 1 is a structural diagram of the bevel gear shaft milling tooth elastic positioning and locking device of the present invention.
具体实施方式:Detailed ways:
由图1可知,锥齿轮轴铣齿弹性定位锁紧装置由铣齿胎体1、套筒2、锁紧弹簧套3、丝堵4、定位弹簧套5组成。铣齿胎体1右端与套筒2左半部为螺纹配合联接在一起;带开口槽的锁紧弹簧套3放入套筒2内,锁紧弹簧套3与套筒2前后各有一段设为间隙配合接触,套筒2左端与锁紧弹簧套3左端锥面配合,且锁紧弹簧套3左端外锥面可沿套筒2左端内锥面轴向移动;丝堵4一端与锁紧弹簧套3为螺纹配合联接在一起;铣齿胎体1前端装有带开口槽的定位弹簧套5,铣齿胎体1前端内孔锥度与定位弹簧套5外圆锥度一致,采用配磨加工;锥齿轮轴6装入铣齿胎体1内孔中,铣齿胎体1用螺栓固定在机床主轴端面上;丝堵4另一端与机床油压系统联接。It can be seen from Fig. 1 that the elastic positioning and locking device for bevel gear shaft milling is composed of a milling carcass 1, a sleeve 2, a
工作时,先将铣齿胎体1用螺栓固定在机床主轴端面上,丝堵4另一端与机床油压系统联接。将工件6擦拭干净轻轻装入定位弹簧套5内孔中,当机床给出油压时丝堵4带动锁紧弹簧套3向右移动,由于套筒2是固定不动的,锁紧弹簧套3在斜面作用下使开口槽收缩,先将工件自动锁紧,后带动工件6一起向右移动,工件6向右移动将定位弹簧套5压紧涨开,消除了铣齿胎体1与定位弹簧套5、工件6与定位弹簧套5之间的间隙,起到精确定位作用,此时即可进行工件6的加工,当工件加工成后,松开油压,丝堵4与锁紧弹簧套3同时失去外力,将工件松开,工件松开后定位弹簧套5失去作用,便可将工件取出。During work, the milling tooth carcass 1 is fixed on the end face of the main shaft of the machine tool with bolts, and the other end of the
应当理解,以上借助优选实施例对本发明的技术方案进行的详细说明是示意性的而非限制性的。本领域的普通技术人员在阅读本发明说明书的基础上可以对实施例所记载的技术方案进行修改,或者对其中部分技术特征进行等同替换;而这些修改或者替换,并不使相应技术方案的本质脱离本发明实施例技术方案的精神和范围。It should be understood that the above detailed description of the technical solution of the present invention with the aid of preferred embodiments is illustrative rather than restrictive. Those skilled in the art can modify the technical solutions described in the embodiments on the basis of reading the description of the present invention, or perform equivalent replacements for some of the technical features; and these modifications or replacements do not make the essence of the corresponding technical solutions Deviate from the spirit and scope of the technical solutions of the embodiments of the present invention.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2013102020999A CN103406603A (en) | 2013-05-17 | 2013-05-17 | Elastic locating and locking device for milled teeth of bevel gear shaft |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2013102020999A CN103406603A (en) | 2013-05-17 | 2013-05-17 | Elastic locating and locking device for milled teeth of bevel gear shaft |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN103406603A true CN103406603A (en) | 2013-11-27 |
Family
ID=49599670
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2013102020999A Pending CN103406603A (en) | 2013-05-17 | 2013-05-17 | Elastic locating and locking device for milled teeth of bevel gear shaft |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN103406603A (en) |
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105562749A (en) * | 2016-02-29 | 2016-05-11 | 宝鸡石油机械有限责任公司 | Automotive clamping method for elastic sealing backing ring |
| CN105562836A (en) * | 2014-11-07 | 2016-05-11 | 綦江县飞达重型汽车齿轮厂 | Chamfer grinding machining device for gear tooth ends of gear shaft |
| CN105618863A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Precise positioning tool for grinding end chamfer of gear tooth of gear shaft |
| CN105618870A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Axial part stepping rotation clamping tooling |
| CN105618866A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Rotary location type gear shaft gear tooth end chamfering grinding processing device |
| CN105618864A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Gear shaft gear tooth end chamfering and grinding tooling |
| CN106180914A (en) * | 2016-08-31 | 2016-12-07 | 宁波菲仕运动控制技术有限公司 | A kind of female splined shaft gear-shaping clamp |
Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2935329A (en) * | 1959-05-20 | 1960-05-03 | Gleason Works | Chuck and collet therefor |
| US3674280A (en) * | 1970-12-16 | 1972-07-04 | Gleason Works | Self-cleaning chuck |
| CN201211581Y (en) * | 2008-06-20 | 2009-03-25 | 江苏飞船股份有限公司 | Bevel gear shaft double-positioning supporting gear milling fixture |
| CN101722339A (en) * | 2009-12-14 | 2010-06-09 | 江苏飞船股份有限公司 | Gear milling positioning fixture for spiral bevel gear |
| CN102380821A (en) * | 2011-10-28 | 2012-03-21 | 江苏上齿集团有限公司 | Bevel gear shaft dual-positioning grinding fixture |
| CN202224777U (en) * | 2011-09-09 | 2012-05-23 | 江苏飞船股份有限公司 | Purification structure of end surface finishing tooth jig |
| CN202845960U (en) * | 2012-10-17 | 2013-04-03 | 重庆市星极齿轮有限责任公司 | Gear grinding clamp for gear shaft with large aperture |
| CN203343557U (en) * | 2013-05-17 | 2013-12-18 | 中煤张家口煤矿机械有限责任公司 | Gear milling elastic positioning and clamping device for bevel gear shaft |
-
2013
- 2013-05-17 CN CN2013102020999A patent/CN103406603A/en active Pending
Patent Citations (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US2935329A (en) * | 1959-05-20 | 1960-05-03 | Gleason Works | Chuck and collet therefor |
| US3674280A (en) * | 1970-12-16 | 1972-07-04 | Gleason Works | Self-cleaning chuck |
| CN201211581Y (en) * | 2008-06-20 | 2009-03-25 | 江苏飞船股份有限公司 | Bevel gear shaft double-positioning supporting gear milling fixture |
| CN101722339A (en) * | 2009-12-14 | 2010-06-09 | 江苏飞船股份有限公司 | Gear milling positioning fixture for spiral bevel gear |
| CN202224777U (en) * | 2011-09-09 | 2012-05-23 | 江苏飞船股份有限公司 | Purification structure of end surface finishing tooth jig |
| CN102380821A (en) * | 2011-10-28 | 2012-03-21 | 江苏上齿集团有限公司 | Bevel gear shaft dual-positioning grinding fixture |
| CN202845960U (en) * | 2012-10-17 | 2013-04-03 | 重庆市星极齿轮有限责任公司 | Gear grinding clamp for gear shaft with large aperture |
| CN203343557U (en) * | 2013-05-17 | 2013-12-18 | 中煤张家口煤矿机械有限责任公司 | Gear milling elastic positioning and clamping device for bevel gear shaft |
Cited By (9)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN105562836A (en) * | 2014-11-07 | 2016-05-11 | 綦江县飞达重型汽车齿轮厂 | Chamfer grinding machining device for gear tooth ends of gear shaft |
| CN105618863A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Precise positioning tool for grinding end chamfer of gear tooth of gear shaft |
| CN105618870A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Axial part stepping rotation clamping tooling |
| CN105618866A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Rotary location type gear shaft gear tooth end chamfering grinding processing device |
| CN105618864A (en) * | 2014-11-07 | 2016-06-01 | 綦江县飞达重型汽车齿轮厂 | Gear shaft gear tooth end chamfering and grinding tooling |
| CN105618870B (en) * | 2014-11-07 | 2018-03-16 | 綦江县飞达重型汽车齿轮厂 | Shaft forgings stepping rotates clamping tooling |
| CN105562749A (en) * | 2016-02-29 | 2016-05-11 | 宝鸡石油机械有限责任公司 | Automotive clamping method for elastic sealing backing ring |
| CN105562749B (en) * | 2016-02-29 | 2017-10-31 | 宝鸡石油机械有限责任公司 | A kind of automobile-used clamping method of elastic packing gasket ring |
| CN106180914A (en) * | 2016-08-31 | 2016-12-07 | 宁波菲仕运动控制技术有限公司 | A kind of female splined shaft gear-shaping clamp |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN104525982A (en) | Rotating center of lathe center rest | |
| CN202192508U (en) | Elastic positioning external grinding mandrel with high precision | |
| CN103737123A (en) | Gear shaving tool | |
| CN204182936U (en) | A kind of centre with endlong movement mechanism | |
| CN104001949A (en) | Multi-cutter-station cutter disk frame | |
| CN204449450U (en) | Molding cutter | |
| CN203343557U (en) | Gear milling elastic positioning and clamping device for bevel gear shaft | |
| CN104400617B (en) | A kind of high-precision elongated hole directive property lappingout lap tool and Ginding process | |
| CN203751800U (en) | Machining device directly clamping threaded surface without damaging thread | |
| CN203956140U (en) | A kind of Special-purpose machine tool for boring | |
| CN103537764A (en) | Rotary scraping tool | |
| CN204450017U (en) | Swivel nut inner bore of part lathe for machining fixture | |
| CN204430317U (en) | Lathe precision centering collet tube | |
| CN104625124A (en) | Radial adjustable deep-hole boring cutter for guide blocks | |
| CN204470626U (en) | A kind of guide pad radial adjustable deep-hole boring cutter | |
| CN103406718A (en) | Gyratory cutting double-faced simultaneous machining method | |
| CN203636379U (en) | Seamless clamping positioning device for thin-wall external threads | |
| CN205147508U (en) | Differential side gear garland key positioning fixture | |
| CN204397092U (en) | A kind of internal-expansion type clamping device | |
| CN204381408U (en) | The fit structure of lathe spindle sleeve and main spindle box | |
| CN104191049B (en) | External screw thread shaft member processing method | |
| CN204339539U (en) | Anistree groove sealing surface grinding aid | |
| CN207914615U (en) | A kind of Internal hole positioning machining tool | |
| CN203594461U (en) | Guide sleeve of hydraulic support stand column | |
| CN206936459U (en) | A kind of drilling angle flange device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C02 | Deemed withdrawal of patent application after publication (patent law 2001) | ||
| WD01 | Invention patent application deemed withdrawn after publication |
Application publication date: 20131127 |