CN102737760A - Reinforced tensile screening type vertical watertight degaussing cable for ship and manufacturing method thereof - Google Patents
Reinforced tensile screening type vertical watertight degaussing cable for ship and manufacturing method thereof Download PDFInfo
- Publication number
- CN102737760A CN102737760A CN2012102038428A CN201210203842A CN102737760A CN 102737760 A CN102737760 A CN 102737760A CN 2012102038428 A CN2012102038428 A CN 2012102038428A CN 201210203842 A CN201210203842 A CN 201210203842A CN 102737760 A CN102737760 A CN 102737760A
- Authority
- CN
- China
- Prior art keywords
- rubber
- parts
- periphery
- cable core
- plasticizer
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Granted
Links
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 13
- 238000012216 screening Methods 0.000 title abstract 2
- 229920001971 elastomer Polymers 0.000 claims abstract description 156
- 239000000565 sealant Substances 0.000 claims abstract description 54
- 239000004020 conductor Substances 0.000 claims abstract description 50
- 238000004073 vulcanization Methods 0.000 claims abstract description 47
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims abstract description 42
- 229910052802 copper Inorganic materials 0.000 claims abstract description 30
- 239000010949 copper Substances 0.000 claims abstract description 30
- 229920006231 aramid fiber Polymers 0.000 claims abstract description 26
- 229920001084 poly(chloroprene) Polymers 0.000 claims abstract description 19
- 239000003795 chemical substances by application Substances 0.000 claims description 78
- 239000004014 plasticizer Substances 0.000 claims description 69
- 238000002156 mixing Methods 0.000 claims description 63
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 claims description 57
- 230000003213 activating effect Effects 0.000 claims description 53
- 239000000945 filler Substances 0.000 claims description 41
- XLOMVQKBTHCTTD-UHFFFAOYSA-N Zinc monoxide Chemical compound [Zn]=O XLOMVQKBTHCTTD-UHFFFAOYSA-N 0.000 claims description 40
- 239000012763 reinforcing filler Substances 0.000 claims description 37
- 229920002943 EPDM rubber Polymers 0.000 claims description 36
- 238000009413 insulation Methods 0.000 claims description 35
- 239000003063 flame retardant Substances 0.000 claims description 32
- 239000000463 material Substances 0.000 claims description 30
- CPLXHLVBOLITMK-UHFFFAOYSA-N Magnesium oxide Chemical compound [Mg]=O CPLXHLVBOLITMK-UHFFFAOYSA-N 0.000 claims description 26
- FPAFDBFIGPHWGO-UHFFFAOYSA-N dioxosilane;oxomagnesium;hydrate Chemical compound O.[Mg]=O.[Mg]=O.[Mg]=O.O=[Si]=O.O=[Si]=O.O=[Si]=O.O=[Si]=O FPAFDBFIGPHWGO-UHFFFAOYSA-N 0.000 claims description 26
- 238000001816 cooling Methods 0.000 claims description 25
- 238000009954 braiding Methods 0.000 claims description 24
- 239000011787 zinc oxide Substances 0.000 claims description 20
- QIQXTHQIDYTFRH-UHFFFAOYSA-N octadecanoic acid Chemical compound CCCCCCCCCCCCCCCCCC(O)=O QIQXTHQIDYTFRH-UHFFFAOYSA-N 0.000 claims description 19
- 235000021355 Stearic acid Nutrition 0.000 claims description 18
- OQCDKBAXFALNLD-UHFFFAOYSA-N octadecanoic acid Natural products CCCCCCCC(C)CCCCCCCCC(O)=O OQCDKBAXFALNLD-UHFFFAOYSA-N 0.000 claims description 18
- 239000000377 silicon dioxide Substances 0.000 claims description 18
- 239000008117 stearic acid Substances 0.000 claims description 18
- BJQHLKABXJIVAM-UHFFFAOYSA-N bis(2-ethylhexyl) phthalate Chemical compound CCCCC(CC)COC(=O)C1=CC=CC=C1C(=O)OCC(CC)CCCC BJQHLKABXJIVAM-UHFFFAOYSA-N 0.000 claims description 17
- 239000008119 colloidal silica Substances 0.000 claims description 17
- 239000003517 fume Substances 0.000 claims description 17
- KOMNUTZXSVSERR-UHFFFAOYSA-N 1,3,5-tris(prop-2-enyl)-1,3,5-triazinane-2,4,6-trione Chemical compound C=CCN1C(=O)N(CC=C)C(=O)N(CC=C)C1=O KOMNUTZXSVSERR-UHFFFAOYSA-N 0.000 claims description 16
- YHMYGUUIMTVXNW-UHFFFAOYSA-N 1,3-dihydrobenzimidazole-2-thione Chemical compound C1=CC=C2NC(S)=NC2=C1 YHMYGUUIMTVXNW-UHFFFAOYSA-N 0.000 claims description 16
- 238000005987 sulfurization reaction Methods 0.000 claims description 16
- 229910000410 antimony oxide Inorganic materials 0.000 claims description 15
- VTRUBDSFZJNXHI-UHFFFAOYSA-N oxoantimony Chemical compound [Sb]=O VTRUBDSFZJNXHI-UHFFFAOYSA-N 0.000 claims description 15
- 239000002994 raw material Substances 0.000 claims description 15
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 claims description 15
- XMNIXWIUMCBBBL-UHFFFAOYSA-N 2-(2-phenylpropan-2-ylperoxy)propan-2-ylbenzene Chemical compound C=1C=CC=CC=1C(C)(C)OOC(C)(C)C1=CC=CC=C1 XMNIXWIUMCBBBL-UHFFFAOYSA-N 0.000 claims description 14
- 239000004215 Carbon black (E152) Substances 0.000 claims description 14
- 239000005662 Paraffin oil Substances 0.000 claims description 14
- 238000013459 approach Methods 0.000 claims description 14
- AFZSMODLJJCVPP-UHFFFAOYSA-N dibenzothiazol-2-yl disulfide Chemical compound C1=CC=C2SC(SSC=3SC4=CC=CC=C4N=3)=NC2=C1 AFZSMODLJJCVPP-UHFFFAOYSA-N 0.000 claims description 14
- DMBHHRLKUKUOEG-UHFFFAOYSA-N diphenylamine Chemical class C=1C=CC=CC=1NC1=CC=CC=C1 DMBHHRLKUKUOEG-UHFFFAOYSA-N 0.000 claims description 14
- 229930195733 hydrocarbon Natural products 0.000 claims description 14
- 150000002430 hydrocarbons Chemical class 0.000 claims description 14
- 239000004200 microcrystalline wax Substances 0.000 claims description 14
- 235000019808 microcrystalline wax Nutrition 0.000 claims description 14
- 238000012856 packing Methods 0.000 claims description 14
- 238000007789 sealing Methods 0.000 claims description 14
- BOXSVZNGTQTENJ-UHFFFAOYSA-L zinc dibutyldithiocarbamate Chemical compound [Zn+2].CCCCN(C([S-])=S)CCCC.CCCCN(C([S-])=S)CCCC BOXSVZNGTQTENJ-UHFFFAOYSA-L 0.000 claims description 14
- 239000002202 Polyethylene glycol Substances 0.000 claims description 13
- 239000000395 magnesium oxide Substances 0.000 claims description 13
- 229920001223 polyethylene glycol Polymers 0.000 claims description 13
- VTHJTEIRLNZDEV-UHFFFAOYSA-L magnesium dihydroxide Chemical compound [OH-].[OH-].[Mg+2] VTHJTEIRLNZDEV-UHFFFAOYSA-L 0.000 claims description 12
- 239000000347 magnesium hydroxide Substances 0.000 claims description 12
- 229910001862 magnesium hydroxide Inorganic materials 0.000 claims description 12
- 239000012530 fluid Substances 0.000 claims description 11
- 230000036760 body temperature Effects 0.000 claims description 10
- 230000004927 fusion Effects 0.000 claims description 10
- 239000003292 glue Substances 0.000 claims description 10
- 238000002360 preparation method Methods 0.000 claims description 9
- 238000005728 strengthening Methods 0.000 claims description 8
- 238000007599 discharging Methods 0.000 claims description 5
- 238000005470 impregnation Methods 0.000 claims description 5
- 230000005855 radiation Effects 0.000 claims description 5
- 238000004513 sizing Methods 0.000 claims description 5
- 238000007598 dipping method Methods 0.000 claims description 4
- 230000000694 effects Effects 0.000 abstract description 11
- 239000012466 permeate Substances 0.000 abstract 1
- 230000003014 reinforcing effect Effects 0.000 abstract 1
- 238000002791 soaking Methods 0.000 abstract 1
- 239000000047 product Substances 0.000 description 21
- 230000032683 aging Effects 0.000 description 20
- 238000006073 displacement reaction Methods 0.000 description 12
- 230000008595 infiltration Effects 0.000 description 12
- 238000001764 infiltration Methods 0.000 description 12
- 239000000126 substance Substances 0.000 description 12
- 238000012360 testing method Methods 0.000 description 11
- 239000012188 paraffin wax Substances 0.000 description 10
- 238000005336 cracking Methods 0.000 description 8
- 239000003921 oil Substances 0.000 description 8
- 239000013535 sea water Substances 0.000 description 8
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 description 7
- 239000001301 oxygen Substances 0.000 description 7
- 229910052760 oxygen Inorganic materials 0.000 description 7
- CBENFWSGALASAD-UHFFFAOYSA-N Ozone Chemical compound [O-][O+]=O CBENFWSGALASAD-UHFFFAOYSA-N 0.000 description 6
- 230000007797 corrosion Effects 0.000 description 6
- 238000005260 corrosion Methods 0.000 description 6
- 238000007654 immersion Methods 0.000 description 6
- 230000005347 demagnetization Effects 0.000 description 5
- ZAMOUSCENKQFHK-UHFFFAOYSA-N Chlorine atom Chemical compound [Cl] ZAMOUSCENKQFHK-UHFFFAOYSA-N 0.000 description 4
- 229920000181 Ethylene propylene rubber Polymers 0.000 description 4
- FAPWRFPIFSIZLT-UHFFFAOYSA-M Sodium chloride Chemical compound [Na+].[Cl-] FAPWRFPIFSIZLT-UHFFFAOYSA-M 0.000 description 4
- 239000000460 chlorine Substances 0.000 description 4
- 229910052801 chlorine Inorganic materials 0.000 description 4
- 150000003254 radicals Chemical class 0.000 description 4
- 238000005516 engineering process Methods 0.000 description 3
- 239000012744 reinforcing agent Substances 0.000 description 3
- OWRCNXZUPFZXOS-UHFFFAOYSA-N 1,3-diphenylguanidine Chemical compound C=1C=CC=CC=1NC(=N)NC1=CC=CC=C1 OWRCNXZUPFZXOS-UHFFFAOYSA-N 0.000 description 2
- RNFJDJUURJAICM-UHFFFAOYSA-N 2,2,4,4,6,6-hexaphenoxy-1,3,5-triaza-2$l^{5},4$l^{5},6$l^{5}-triphosphacyclohexa-1,3,5-triene Chemical compound N=1P(OC=2C=CC=CC=2)(OC=2C=CC=CC=2)=NP(OC=2C=CC=CC=2)(OC=2C=CC=CC=2)=NP=1(OC=1C=CC=CC=1)OC1=CC=CC=C1 RNFJDJUURJAICM-UHFFFAOYSA-N 0.000 description 2
- FYYHWMGAXLPEAU-UHFFFAOYSA-N Magnesium Chemical compound [Mg] FYYHWMGAXLPEAU-UHFFFAOYSA-N 0.000 description 2
- UTGQNNCQYDRXCH-UHFFFAOYSA-N N,N'-diphenyl-1,4-phenylenediamine Chemical compound C=1C=C(NC=2C=CC=CC=2)C=CC=1NC1=CC=CC=C1 UTGQNNCQYDRXCH-UHFFFAOYSA-N 0.000 description 2
- 230000003712 anti-aging effect Effects 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 2
- 238000006243 chemical reaction Methods 0.000 description 2
- 238000009792 diffusion process Methods 0.000 description 2
- 239000012535 impurity Substances 0.000 description 2
- 239000011777 magnesium Substances 0.000 description 2
- 229910052749 magnesium Inorganic materials 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- RLLPVAHGXHCWKJ-UHFFFAOYSA-N permethrin Chemical compound CC1(C)C(C=C(Cl)Cl)C1C(=O)OCC1=CC=CC(OC=2C=CC=CC=2)=C1 RLLPVAHGXHCWKJ-UHFFFAOYSA-N 0.000 description 2
- 238000012545 processing Methods 0.000 description 2
- 239000011780 sodium chloride Substances 0.000 description 2
- APLGXMKUJWCEBP-UHFFFAOYSA-N 1-butoxy-4-[(4-methylphenyl)methoxy]benzene Chemical compound C1=CC(OCCCC)=CC=C1OCC1=CC=C(C)C=C1 APLGXMKUJWCEBP-UHFFFAOYSA-N 0.000 description 1
- VXEGSRKPIUDPQT-UHFFFAOYSA-N 4-[4-(4-methoxyphenyl)piperazin-1-yl]aniline Chemical compound C1=CC(OC)=CC=C1N1CCN(C=2C=CC(N)=CC=2)CC1 VXEGSRKPIUDPQT-UHFFFAOYSA-N 0.000 description 1
- MQIUGAXCHLFZKX-UHFFFAOYSA-N Di-n-octyl phthalate Natural products CCCCCCCCOC(=O)C1=CC=CC=C1C(=O)OCCCCCCCC MQIUGAXCHLFZKX-UHFFFAOYSA-N 0.000 description 1
- 241000196324 Embryophyta Species 0.000 description 1
- PEDCQBHIVMGVHV-UHFFFAOYSA-N Glycerine Chemical compound OCC(O)CO PEDCQBHIVMGVHV-UHFFFAOYSA-N 0.000 description 1
- 239000006057 Non-nutritive feed additive Substances 0.000 description 1
- GWEVSGVZZGPLCZ-UHFFFAOYSA-N Titan oxide Chemical compound O=[Ti]=O GWEVSGVZZGPLCZ-UHFFFAOYSA-N 0.000 description 1
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 1
- 239000002253 acid Substances 0.000 description 1
- 239000000654 additive Substances 0.000 description 1
- 230000000996 additive effect Effects 0.000 description 1
- -1 age resistor Substances 0.000 description 1
- 229910052787 antimony Inorganic materials 0.000 description 1
- WATWJIUSRGPENY-UHFFFAOYSA-N antimony atom Chemical compound [Sb] WATWJIUSRGPENY-UHFFFAOYSA-N 0.000 description 1
- 239000003963 antioxidant agent Substances 0.000 description 1
- 230000003078 antioxidant effect Effects 0.000 description 1
- 239000012752 auxiliary agent Substances 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 239000003990 capacitor Substances 0.000 description 1
- 239000006229 carbon black Substances 0.000 description 1
- 239000007822 coupling agent Substances 0.000 description 1
- 230000002708 enhancing effect Effects 0.000 description 1
- 239000012467 final product Substances 0.000 description 1
- 239000012847 fine chemical Substances 0.000 description 1
- 150000004820 halides Chemical class 0.000 description 1
- 229920002681 hypalon Polymers 0.000 description 1
- 229910052500 inorganic mineral Inorganic materials 0.000 description 1
- 239000011810 insulating material Substances 0.000 description 1
- 239000011159 matrix material Substances 0.000 description 1
- 239000005055 methyl trichlorosilane Substances 0.000 description 1
- JLUFWMXJHAVVNN-UHFFFAOYSA-N methyltrichlorosilane Chemical compound C[Si](Cl)(Cl)Cl JLUFWMXJHAVVNN-UHFFFAOYSA-N 0.000 description 1
- 239000011707 mineral Substances 0.000 description 1
- 239000002105 nanoparticle Substances 0.000 description 1
- 150000002885 octadecanoids Chemical class 0.000 description 1
- 238000011056 performance test Methods 0.000 description 1
- 239000003208 petroleum Substances 0.000 description 1
- 229920003023 plastic Polymers 0.000 description 1
- 239000004033 plastic Substances 0.000 description 1
- 239000000843 powder Substances 0.000 description 1
- 239000011164 primary particle Substances 0.000 description 1
- 229910052710 silicon Inorganic materials 0.000 description 1
- 239000010703 silicon Substances 0.000 description 1
- 239000005049 silicon tetrachloride Substances 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
- 230000035882 stress Effects 0.000 description 1
- 235000010215 titanium dioxide Nutrition 0.000 description 1
- 229910052613 tourmaline Inorganic materials 0.000 description 1
- 229940070527 tourmaline Drugs 0.000 description 1
- 239000011032 tourmaline Substances 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
- 239000011701 zinc Substances 0.000 description 1
- 229910052725 zinc Inorganic materials 0.000 description 1
Images
Landscapes
- Organic Insulating Materials (AREA)
- Sealing Material Composition (AREA)
- Insulated Conductors (AREA)
- Compositions Of Macromolecular Compounds (AREA)
Abstract
The invention discloses a reinforced tensile screening type vertical watertight degaussing cable for a ship and a manufacturing method thereof. A twisted copper conductor is formed by soaking a plurality of tinned copper wires in a sealant and then twisting the tinned copper wires; a conductor sealant layer is soaked on the periphery of the twisted copper conductor; insulating rubber layers are extruded on the periphery of the conductor sealant layer; an aramid fiber reinforcing layer is weaved on the periphery of each insulating rubber layer so as to form an insulating core wire; chloroprene rubber filling strips are filled into gaps among the insulating core wires, and a cable core is integrally formed by twisting the insulating core wires; a cable core inner sealant layer is extruded on the periphery of the cable core; and an inner jacket rubber layer is extruded on the periphery of the cable core inner sealant layer. A plurality of seals are arranged on the periphery of a cable conductor, and the chloroprene rubber filling strips expand in a follow-up vulcanization process, thus entirely filling the gaps in the cable core; and one insulating core wire is not tangential to another insulating core wire. Therefore, when the cable core inner sealant layer is extruded, the sealant can permeate inside the cable core, so that the watertight effect can be ensured.
Description
Technical field
The present invention relates to a kind of cable, particularly a kind of naval vessel is with strengthening tension shield type direction waterproof degaussing cable; The invention still further relates to a kind of naval vessel with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable.
Background technology
The naval vessel especially under water the naval vessel in underway because of stealthy importance, to prevent that especially magnetic mine from attacking, need often carry out the hull demagnetization for this reason.Fixedly demagnetization is carried out demagnetization at degaussing stations and is got final product, but just need by self ship side outer eraser system of installing carry out demagnetization for the induced field that the naval vessel produced that is in for a long time in the underway under water.But because the particularity and the complexity of ship navigation environment under water, common degaussing cable can't satisfy simultaneously that ship side is outer installs the specification requirement that required longitudinal sealing and demagnetization performance possess simultaneously.
In the electro-insulating rubber industry, ethylene propylene diene rubber K21, the ethylene propylene diene rubber 4045M of arriving commonly used also uses various vulcanizing agents, age resistor, and wherein the vulcanizing agent cumyl peroxide is claimed vulcanizing agent DCP, molecular formula C18H22O2 again; The vulcanization accelerator iso-cyanuric acid triallyl ester is claimed vulcanization accelerator TAIC again, and the age resistor 2 mercapto benzimidazole is claimed antioxidant MB again, age resistor 2,2, and 4-trimethyl-1,2-dihyaroquinoline condensate is claimed anti-aging agent RD again.
In the jacket rubber industry, commonly used to CSM H40; Also use various vulcanizing agents, activating agent, age resistor, plasticizer, fire retardant and filler.The vulcanization accelerator dibenzothiazyl disulfide is claimed vulcanizing agent DM again, and molecular formula is C14H8N2S4; Vulcanization accelerator six sulfuration di-penta methylene thiurams are claimed accelerator D PTT again; The age resistor nickel dibutyl dithiocarbamate is claimed antioxidant NBC again, and molecular formula is C18H36N2S4Ni, and molecular weight is 467.51; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines claims antioxidant H S-911 again, releases in 2005 by Huangyan, Zhejiang China star laboratory; The plasticizer phthalic acid dioctyl ester is claimed plasticizer DOP again.
White carbon is divided into precipitated silica and fume colloidal silica by production method.Be the gluey nano particle of the amorphous cotton-shaped translucent solid of white under the white carbon normality, primary particle diameter is between 7~80nm, and specific area is generally greater than 100 ㎡/g.By halide (mainly being silicon tetrachloride and methyl trichlorosilane) the nanoscale white powder that pyrohydrolysis generates in oxyhydrogen flame of silicon, mainly as reinforced filling and multifunction additive.
Publication number is that the patent of invention of CN 102408636A discloses a kind of degaussing cable insulating material and preparation method thereof; It adopts ethylene-propylene rubber TER4044 and EBM4050 as the rubber matrix; And be main with TER4044; As plasticizer, have good electric insulation and mechanical strength with paraffin wax fully refined, paraffin oil and microcrystalline wax.Ethylene-propylene rubber is fire-retardant thinks that ability is relatively poor, and oxygen index is usually less than 26, and fire resistance is bad.
Publication number is that the patent of invention of CN 102417639A discloses corrosion-resistant sheath material of a kind of degaussing cable waterproof and preparation method thereof, has adopted 100 parts of neoprenes, vulcanizing agent 5-20 part, vulcanization accelerator 0.5-5 part, vulcanization aid 0.5-5 part, filler 50-120 part, reinforcing agent 15-10 part, age resistor 1-5 part, plasticizer 5-15 part, fire retardant 5-20 part, coupling agent 1-5 part, processing aid 2-6 part.This sheath material adopts neoprene; The sea water corrosion resistant of neoprene is well below chlorosulfonated polyethylene; This sheath material is only realized immersing seawater and is born after 14 days that withstand voltage (7kV 5min) does not puncture, on water resistance radially; Can only bear 0.5MPa air pressure, (7kV 5min) does not puncture proof voltage.
Summary of the invention
Primary and foremost purpose of the present invention is, overcomes the problem that exists in the prior art, provides a kind of naval vessel with strengthening tension shield type direction waterproof degaussing cable, and mechanical performance and watertightness performance are superior, and insulation is reliable, and oil resistant, corrosion-resistant, and shield effectiveness is good.
For solving above technical problem; A kind of naval vessel provided by the present invention is with strengthening tension shield type direction waterproof degaussing cable; The stranded twisted copper conductors that becomes behind the many tinned copper wire dipping fluid sealants; Said twisted copper conductors periphery is impregnated with the conductor sealant layer, and the periphery of said conductor sealant layer is extruded with the electro-insulating rubber layer, and the periphery of said electro-insulating rubber layer is woven with aramid fiber silk reinforced layer and constitutes the insulation heart yearn; Place, slit between each said insulation heart yearn is filled with the neoprene packing and many said insulation heart yearn integral body are twisted into cable core; The periphery of said cable core is extruded with sealant layer in the cable core, and the periphery of sealant layer is extruded with the inner sheath rubber layer in the said cable core, and the periphery of said inner sheath rubber layer is woven with the armouring screen; The periphery of said armouring screen is extruded with cable core external seal glue-line, and the periphery of said cable core external seal glue-line is extruded with the oversheath rubber layer.
With respect to prior art, the present invention has obtained following beneficial effect: conductor monofilament dipping fluid sealant, and the twisted copper conductors periphery is impregnated with the conductor sealant layer; The periphery of cable core is extruded with sealant layer in the cable core; Formed multi-sealedly, the slit place of insulation between the heart yearn is filled with the neoprene packing, the neoprene packing slit in can the complete filling cable core of when follow-up sulfuration, expanding; And can cause between insulation heart yearn and the insulation heart yearn no longer tangent; Thereby make when extruding in the cable core sealant layer, fluid sealant can penetrate into cable core inside, guarantees the watertight effect; Every insulated heart yearn periphery is woven with aramid fiber silk reinforced layer, and tensile strength is high; The cable core periphery also is provided with armouring screen, cable core external seal glue-line and oversheath rubber layer, and shield effectiveness, sealing property and anticorrosion effect are better.
As the present invention is preferred version, and the filament diameter of said twisted copper conductors is 0.2~0.4mm, is twisted into strand with 8~10 times lay ratios, and said strand is twisted into said twisted copper conductors according to the direction opposite with former bundle strand with 12~16 times lay ratio more again; The stranded lay ratio of said cable core is 18~20 times; The coefficient of expansion of said neoprene packing is 1.1~1.2; Said aramid fiber silk reinforced layer is that the aramid fiber silk braiding of 0.15~0.2mm forms by diameter; The hot strength of said aramid fiber silk is 3000MPa~4000MPa; Modulus of elasticity is 100GPa~200GPa, and angle of weave is between 30 °~50 °, and percentage of braiding coverage is 30%~45%; Said armouring screen is that the tinned copper wire braiding of 0.3mm forms by diameter, and angle of weave is 40 °~60 °, and percentage of braiding coverage is 88%~92%.
As preferred version of the present invention, the raw material components and the weight content of said electro-insulating rubber layer are following: ethylene propylene diene rubber K21:15 part; Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.5~0.6 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.2~0.3 part; Age resistor 2 mercapto benzimidazole: 0.7~0.9 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.2~0.3 part; Plasticizer paraffin oil: 1.0~2.0 parts; Plasticizer chlorinated paraffin-52: 1~2 part; Plasticizer microcrystalline wax: 0.5~1.0 part; Activating agent zinc oxide: 1.0~2.0 parts; Activating agent stearic acid: 0.3~0.5 part; Filler superfine talcum powder: 8~11 parts; Reinforcing filler fume colloidal silica: 1.0~1.5 parts; Reinforcing filler calcinated argil: 7~9 parts.The present invention adopts ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M mixing; The Mooney viscosity of ethylene propylene diene rubber K21 is lower, and plasticity is good, can guarantee the flexibility requirement of rubber; And ethylene propylene diene rubber 4045M Mooney viscosity is higher; Rubber tensile strength is big, and the two is mixing can to realize combination property of soft and high mechanical properties, and on cost far below ethylene-propylene rubber TER4044 and EBM4050; Chlorinated paraffin wax is except possessing the plasticising emollescence; The chlorine element that it contains also has fire retardation; Chlorinated paraffin wax substitutes paraffin wax fully refined; Can improve rubber and effectively pounce on the free radical of catching rubber burning generation, play fire retardation, material of the present invention adopts HC-2 limiting oxygen index determination appearance to measure its oxygen index can reach 32.1%; Adopt fume colloidal silica to substitute precipitated silica, can improve the insulation property and the physical and mechanical properties of electro-insulating rubber better as reinforcing agent, and fume colloidal silica is thinner, impurity still less, be easy to mixing processing; Adopt zinc oxide and the agent of stearic acid mixed active, can promote the abundant diffusion of white carbon and zinc oxide, be easy to mixing evenly, and stearic acid and zinc oxide react and can promote activity; Tensile strength before this electro-insulating rubber is aging is greater than 6.5N/mm2; Elongation at break >=290%, insulation resistance can reach more than the 3400 M Ω km, and insulation property and mechanical performance are superior; And ageing-resistant, can satisfy the instructions for use of naval vessel with the direction waterproof degaussing cable.
As preferred version of the present invention, the raw material components and the weight content of said inner sheath rubber layer and oversheath rubber layer are following: CSM H40:20 part; Vulcanization accelerator dibenzothiazyl disulfide: 0.4~0.6 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.3~0.5 part; Activating agent magnesia: 1.0~1.5 parts; Activating agent polyethylene glycol: 1.0~2.0 parts; Age resistor nickel dibutyl dithiocarbamate: 0.2~0.4 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.1~0.2 part; Plasticizer phthalic acid dioctyl ester: 2.5~3.0 parts; Fire retardant antimony oxide: 1~1.5 part; Plasticizer chlorinated paraffin-52: 0.5~1 part; Fire retardant magnesium hydroxide: 1~1.5 part; Filler semi-reinforcing hydrocarbon black: 0.5~1 part; Reinforcing filler precipitated silica: 5.5~6.5 parts; Filler superfine talcum powder: 8~12 parts.Chlorinated paraffin wax is except possessing the plasticising emollescence, and the chlorine element that it contains also has fire retardation, and fire retardant antimony oxide and the reaction of plasticizer chlorinated paraffin-52 can be pounced on and caught the free radical that the rubber burning produces, and play flame retardant effect, improve the oxygen index of rubber; The physical mechanical strength that can improve sheath, the anti-wear performance of Reinforced Rubber are used in filler semi-reinforcing hydrocarbon black and precipitated silica combination; Tensile strength before this jacket rubber is aging can reach more than the 14N/m ㎡, and elongation at break >=330% can realize that the immersion seawater bears after 90 days that withstand voltage (7kV 5min) does not puncture, and bears 3MPa air pressure and withstand voltage (7kV 5min) does not puncture; Mechanical performance is superior, and is ageing-resistant, and oil resistant is corrosion-resistant, and watertightness performance is good, can satisfy the instructions for use of naval vessel with the direction waterproof degaussing cable.
Another object of the present invention is, provides a kind of naval vessel with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable, and cable machinery performance and watertightness performance that this method manufacturing forms are superior, and insulation is reliable, and oil resistant, corrosion-resistant, and shield effectiveness is good.
For solving above technical problem; A kind of naval vessel provided by the present invention is with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable; May further comprise the steps: be that the tinned copper wire of 0.2~0.4mm passes with the speed of 4~5m/s in the sealing glue of fusion earlier, make its surperficial thorough impregnation fluid sealant filament diameter; Again multifilament is twisted into strand with 8~10 times lay ratio, the multiply strand is again according to being twisted into twisted copper conductors with the stranded opposite direction of monofilament again with 12~16 times lay ratio; Said twisted copper conductors is passed with the speed of 30~40m/min in the sealing glue of fusion, extrudes conductor sealant layer and electro-insulating rubber layer simultaneously in the twisted copper conductors periphery then, and said conductor sealant layer is interior, and said electro-insulating rubber layer outside; The periphery braiding aramid fiber silk reinforced layer of said electro-insulating rubber layer constitutes the insulation heart yearn; Place, the slit filling coefficient of expansion between each said insulation heart yearn is 1.1~1.2 neoprene packing; Be 18~20 times with lay ratio then and be twisted into cable core; Then extrude sealant layer and inner sheath rubber layer in the cable core simultaneously in the cable core periphery; Sealant layer is interior in the said cable core, and said inner sheath rubber layer outside; Then at the periphery of inner sheath rubber layer braiding armouring screen, extrude cable core external seal glue-line and oversheath rubber layer simultaneously in the periphery of armouring screen, cable core external seal glue-line is interior, and the oversheath rubber layer is outside.
With respect to prior art, the present invention has obtained following beneficial effect: the cable that this method is made, conductor monofilament dipping fluid sealant; The twisted copper conductors periphery is impregnated with the conductor sealant layer, and the periphery of cable core is extruded with sealant layer in the cable core, has formed multi-sealed; Place, slit between the insulation heart yearn is filled with the neoprene packing; The neoprene packing is in the slit in can the complete filling cable core of expanding of follow-up when sulfuration, and can cause between insulation heart yearn and the insulation heart yearn no longer tangent, thereby make when extruding the interior sealant layer of cable core; Fluid sealant can penetrate into cable core inside, guarantees the watertight effect; Every insulated heart yearn periphery is woven with aramid fiber silk reinforced layer, and tensile strength is high; The cable core periphery also is provided with armouring screen, cable core external seal glue-line and oversheath rubber layer, and sealing and anticorrosion effect are better; The cable core periphery also is provided with armouring screen, cable core external seal glue-line and oversheath rubber layer, and shield effectiveness, sealing property and anticorrosion effect are better.
As preferred version of the present invention, the preparation method of the electro-insulating rubber of said electro-insulating rubber layer is following: raw material, ethylene propylene diene rubber K21:15 part are prepared by following component and weight content in (1); Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.5~0.6 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.2~0.3 part; Age resistor 2 mercapto benzimidazole: 0.7~0.9 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.2~0.3 part; Plasticizer paraffin oil: 1.0~2.0 parts; Plasticizer chlorinated paraffin-52: 1~2 part; Plasticizer microcrystalline wax: 0.5~1.0 part; Activating agent zinc oxide: 1.0~2.0 parts; Activating agent stearic acid: 0.3~0.5 part; Filler superfine talcum powder: 8~11 parts; Reinforcing filler fume colloidal silica: 1.0~1.5 parts; Reinforcing filler calcinated argil: 7~9 parts; (2) be mixing until evenly on 65 ℃~75 ℃ the banbury in temperature earlier with ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M rubber; Add age resistor 2 mercapto benzimidazole, age resistor 2 then successively; 2; 4-trimethyl-1; 2-dihyaroquinoline condensate, plasticizer chlorinated paraffin-52, plasticizer paraffin oil, plasticizer microcrystalline wax, activating agent zinc oxide, activating agent stearic acid, reinforcing filler fume colloidal silica, reinforcing filler calcinated argil and filler superfine talcum powder on banbury mixing 14~16 minutes; Mixing even back is gone up mill and is played the triangle bag eight times, adopts slice behind 20 orders+40 orders+60 orders+80 orders, four metafiltration nets filter rubber then, dries in the air in the space of dried and clean and puts cooling 18~24 hours; Again with mixer mixing on the sizing material 3~5 minutes; In mixing last minute, added vulcanization accelerator iso-cyanuric acid triallyl ester, vulcanizing agent cumyl peroxide successively at interval in 10~20 seconds; Mixingly sheet under the discharging is made a call to behind six triangle bags in mill on the mixing materials after evenly, in the space of dried and clean, continue to dry in the air behind the following sheet put 8~12 hours subsequent use.The present invention adopts ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M mixing; The Mooney viscosity of ethylene propylene diene rubber K21 is lower, and plasticity is good, can guarantee the flexibility requirement of rubber; And ethylene propylene diene rubber 4045M Mooney viscosity is higher; Rubber tensile strength is big, and the two is mixing can to realize combination property of soft and high mechanical properties, and on cost far below ethylene-propylene rubber TER4044 and EBM4050; Chlorinated paraffin wax is except possessing the plasticising emollescence; The chlorine element that it contains also has fire retardation; Chlorinated paraffin wax substitutes paraffin wax fully refined; Can improve rubber and effectively pounce on the free radical of catching rubber burning generation, play fire retardation, material of the present invention adopts HC-2 limiting oxygen index determination appearance to measure its oxygen index can reach 32.1%; Adopt fume colloidal silica to substitute precipitated silica, can improve the insulation property and the physical and mechanical properties of electro-insulating rubber better as reinforcing agent, and fume colloidal silica is thinner, impurity still less, be easy to mixing processing; Adopt zinc oxide and the agent of stearic acid mixed active, can promote the abundant diffusion of white carbon and zinc oxide, be easy to mixing evenly, and stearic acid and zinc oxide react and can promote activity; Tensile strength before this electro-insulating rubber is aging is greater than 6.5N/mm2; Elongation at break >=290%, insulation resistance can reach more than the 3400 M Ω km, and insulation property and mechanical performance are superior; And ageing-resistant, can satisfy the instructions for use of naval vessel with the direction waterproof degaussing cable.
As preferred version of the present invention, 80 ℃ ± 5 ℃ of the head temperatures of rubber extruding machine when said electro-insulating rubber is extruded; Body temperature is 75 ℃ ± 5 ℃; The steam pressure of curing tube is 0.5~0.6MPa, and the rubber extruding machine type of cooling is water cooling.
As preferred version of the present invention, the preparation method of the jacket rubber of said inner sheath rubber layer and oversheath rubber layer is following: raw material, CSM H40:20 part are prepared by following component and weight content in (1); Vulcanization accelerator dibenzothiazyl disulfide: 0.4~0.6 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.3~0.5 part; Activating agent magnesia: 1.0~1.5 parts; Activating agent polyethylene glycol: 1.0~2.0 parts; Age resistor nickel dibutyl dithiocarbamate: 0.2~0.4 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.1~0.2 part; Plasticizer phthalic acid dioctyl ester: 2.5~3.0 parts; Fire retardant antimony oxide: 1~1.5 part; Plasticizer chlorinated paraffin-52: 0.5~1 part; Fire retardant magnesium hydroxide: 1~1.5 part; Filler semi-reinforcing hydrocarbon black: 0.5~1 part; Reinforcing filler precipitated silica: 5.5~6.5 parts; Filler superfine talcum powder: 8~12 parts; (2) be on 75 ℃~85 ℃ the banbury mixing 3~4 minutes in temperature earlier with CSM H40 rubber; Add activating agent magnesia, activating agent polyethylene glycol, fire retardant antimony oxide, filler superfine talcum powder, plasticizer chlorinated paraffin-52, fire retardant magnesium hydroxide, plasticizer phthalic acid dioctyl ester, filler semi-reinforcing hydrocarbon black and reinforcing filler precipitated silica then successively on banbury mixing 4~6 minutes; Then on banbury, add age resistor 4 successively; 4 '-two (α; α-Er Jiajibianji) diphenylamines, vulcanization accelerator dibenzothiazyl disulfide, age resistor nickel dibutyl dithiocarbamate and vulcanization accelerator six sulfuration di-penta methylene thiurams; Formed mixing materials in mixing again 40~60 seconds; The temperature of said mixing materials is controlled at 90 ℃~110 ℃ and move to and approach logical 4~6 heat radiations in the mill, in mill, turns over 8 triangle bags simultaneously, it is 8~10 minutes that whole in mill rolled the material time; Then through the tri-roll press machine slice, institute's slice was fast reduced to 30 ℃~40 ℃ with temperature through chill roll in 15~20 minutes, and in the space of dried and clean, continuing to dry in the air then, it is subsequent use to put more than 10 hours.Chlorinated paraffin wax is except possessing the plasticising emollescence, and the chlorine element that it contains also has fire retardation, and fire retardant antimony oxide and the reaction of plasticizer chlorinated paraffin-52 can be pounced on and caught the free radical that the rubber burning produces, and play flame retardant effect, improve the oxygen index of rubber; The physical mechanical strength that can improve sheath, the anti-wear performance of Reinforced Rubber are used in filler semi-reinforcing hydrocarbon black and precipitated silica combination; Tensile strength before this jacket rubber is aging can reach more than the 14N/m ㎡, and elongation at break >=330% can realize that the immersion seawater bears after 90 days that withstand voltage (7kV 5min) does not puncture, and bears 3MPa air pressure and withstand voltage (7kV 5min) does not puncture; Mechanical performance is superior, and is ageing-resistant, and oil resistant is corrosion-resistant, and watertightness performance is good, can satisfy the instructions for use of naval vessel with the direction waterproof degaussing cable
As preferred version of the present invention; Body temperature when said jacket rubber is extruded is 65 ± 5 ℃; Head temperature is 60 ± 5 ℃, and the extruder temperature type of cooling of rubber extruding machine adopts water cooling, and extruding the back, to adopt pressure be that the pressure of 0.6~0.8MPa vulcanizes; Go out linear velocity and be about 10~12m/min, extruding thickness is 1.8~2.2mm.
Description of drawings
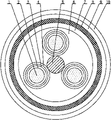
Fig. 1 is the structural representation of naval vessel of the present invention with enhancing tension shield type direction waterproof degaussing cable.
Among the figure: 1. twisted copper conductors, 2. conductor sealant layer, 3. electro-insulating rubber layer, 4. aramid fiber silk reinforced layer, 5. neoprene packing, 6. sealant layer in the cable core, 7. inner sheath rubber layer, 8. armouring screen, 9. cable core external seal glue-line, 10. oversheath rubber layer.
Embodiment
Embodiment one
The preparation electro-insulating rubber is subsequent use earlier, and step is following: raw material is prepared by following component and weight content in (1): ethylene propylene diene rubber K21:15 part; Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.5 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.2 part; Age resistor 2 mercapto benzimidazole: 0.7 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.2 part; Plasticizer paraffin oil: 1.0 parts; Plasticizer chlorinated paraffin-52: 1 part; Plasticizer microcrystalline wax: 0.5 part; Activating agent zinc oxide: 1.0 parts; Activating agent stearic acid: 0.3 part; Filler superfine talcum powder: 8 parts; Reinforcing filler fume colloidal silica: 1.0 parts; Reinforcing filler calcinated argil: 7 parts; (2) be mixing until evenly on 65 ℃ the banbury in temperature earlier with ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M rubber; Add age resistor 2 mercapto benzimidazole, age resistor 2 then successively; 2; 4-trimethyl-1; 2-dihyaroquinoline condensate, plasticizer chlorinated paraffin-52, plasticizer paraffin oil, plasticizer microcrystalline wax, activating agent zinc oxide, activating agent stearic acid, reinforcing filler fume colloidal silica, reinforcing filler calcinated argil and filler superfine talcum powder on banbury mixing 14 minutes; Mixing even back is gone up mill and is played the triangle bag eight times, adopts slice behind 20 orders+40 orders+60 orders+80 orders, four metafiltration nets filter rubber then, dries in the air in the space of dried and clean and puts cooling 18 hours; Again with mixer mixing on the sizing material 3 minutes; In mixing last minute, added vulcanization accelerator iso-cyanuric acid triallyl ester, vulcanizing agent cumyl peroxide successively at interval in 10 seconds; Mixingly sheet under the discharging is made a call to behind six triangle bags in mill on the mixing materials after evenly, in the space of dried and clean, continue to dry in the air behind the following sheet put 8 hours subsequent use.
It is subsequent use to prepare jacket rubber again, and step is following: raw material, CSM H40:20 part are prepared by following component and weight content in (1); Vulcanization accelerator dibenzothiazyl disulfide: 0.4 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.3 part; Activating agent magnesia: 1.0 parts; Activating agent polyethylene glycol: 1.0 parts; Age resistor nickel dibutyl dithiocarbamate: 0.2 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.1 part; Plasticizer phthalic acid dioctyl ester: 2.5 parts; Fire retardant antimony oxide: 1 part; Plasticizer chlorinated paraffin-52: 0.5 part; Fire retardant magnesium hydroxide: 1 part; Filler semi-reinforcing hydrocarbon black: 0.5 part; Reinforcing filler precipitated silica: 5.5 parts; Filler superfine talcum powder: 8 parts; (2) be on 75 ℃ the banbury mixing 3 minutes in temperature earlier with CSM H40 rubber; Add activating agent magnesia, activating agent polyethylene glycol, fire retardant antimony oxide, filler superfine talcum powder, plasticizer chlorinated paraffin-52, fire retardant magnesium hydroxide, plasticizer phthalic acid dioctyl ester, filler semi-reinforcing hydrocarbon black and reinforcing filler precipitated silica then successively on banbury mixing 4 minutes; On banbury, add age resistor 4 then successively; 4 '-two (α; α-Er Jiajibianji) diphenylamines, vulcanization accelerator dibenzothiazyl disulfide, age resistor nickel dibutyl dithiocarbamate and vulcanization accelerator six sulfuration di-penta methylene thiurams; Formed mixing materials in mixing again 40 seconds; The temperature of said mixing materials is controlled at 90 ℃ and move to and approach logical 4 heat radiations in the mill, in mill, turns over 8 triangle bags simultaneously, it is 8 minutes that whole in mill rolled the material time; Then through the tri-roll press machine slice, institute's slice was fast reduced to 40 ℃ with temperature through chill roll in 15 minutes, in the space of dried and clean, continue to dry in the air then put 10 hours subsequent use.
The step of making cable is following: be that the tinned copper wire of 0.2mm passes with the speed of 4m/s in the sealing glue of fusion with filament diameter earlier, make its surperficial thorough impregnation fluid sealant; Again multifilament is twisted into strand with 8 times lay ratio, the multiply strand is again according to being twisted into twisted copper conductors 1 with the stranded opposite direction of monofilament again with 12 times lay ratio; Twisted copper conductors 1 is passed with the speed of 30m/min in the sealing glue of fusion; Extrude conductor sealant layer 2 and electro-insulating rubber layer 3 simultaneously in twisted copper conductors 1 periphery then, conductor sealant layer 2 is interior, and electro-insulating rubber layer 3 outside; The periphery of electro-insulating rubber layer 3 is woven with aramid fiber silk reinforced layer 4 and constitutes the insulation heart yearn; Aramid fiber silk reinforced layer 4 is that the aramid fiber silk braiding of 0.15mm forms by diameter, and the hot strength of aramid fiber silk is 3000MPa, and modulus of elasticity is 100GPa; Angle of weave is 30 °, and percentage of braiding coverage is 30%; Place, the slit filling coefficient of expansion between each insulation heart yearn is 1.1 neoprene packing 5; Be 18 times with lay ratio then and be twisted into cable core; Then extrude sealant layer 6 and armour formula inner sheath rubber layer 7 in the cable core simultaneously in the cable core periphery; Sealant layer 6 is interior in the cable core, and inner sheath rubber layer 7 outside; Then use the tinned copper wire braiding armouring screen 8 of diameter as 0.3mm in the periphery of inner sheath rubber layer 7, angle of weave is 40 °, and percentage of braiding coverage is 88%; Periphery at armouring screen 8 extrudes cable core external seal glue-line 9 and armour formula oversheath rubber layer 10 simultaneously then, and cable core external seal glue-line 9 is interior, and oversheath rubber layer 10 outside.
75 ℃ of the head temperatures of rubber extruding machine when electro-insulating rubber is extruded; Body temperature is 70 ℃; The steam pressure of curing tube is 0.5MPa, and the rubber extruding machine type of cooling is water cooling.
Body temperature when jacket rubber is extruded is 60 ℃, and head temperature is 55 ℃, and the extruder temperature type of cooling of rubber extruding machine adopts water cooling, and extruding the back, to adopt pressure be that the pressure of 0.6MPa vulcanizes, and goes out linear velocity and be about 10m/min, and extruding thickness is 1.8mm.
Embodiment two
The preparation electro-insulating rubber is subsequent use earlier, and step is following: raw material is prepared by following component and weight content in (1): ethylene propylene diene rubber K21:15 part; Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.55 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.25 part; Age resistor 2 mercapto benzimidazole: 0.8 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.25 part; Plasticizer paraffin oil: 1.5 parts; Plasticizer chlorinated paraffin-52: 1.5 parts; Plasticizer microcrystalline wax: 0.8 part; Activating agent zinc oxide: 1.5 parts; Activating agent stearic acid: 0.4 part; Filler superfine talcum powder: 9 parts; Reinforcing filler fume colloidal silica: 1.2 parts; Reinforcing filler calcinated argil: 8 parts; (2) be mixing until evenly on 70 ℃ the banbury in temperature earlier with ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M rubber; Add age resistor 2 mercapto benzimidazole, age resistor 2 then successively; 2; 4-trimethyl-1; 2-dihyaroquinoline condensate, plasticizer chlorinated paraffin-52, plasticizer paraffin oil, plasticizer microcrystalline wax, activating agent zinc oxide, activating agent stearic acid, reinforcing filler fume colloidal silica, reinforcing filler calcinated argil and filler superfine talcum powder on banbury mixing 15 minutes; Mixing even back is gone up mill and is played the triangle bag eight times, adopts slice behind 20 orders+40 orders+60 orders+80 orders, four metafiltration nets filter rubber then, dries in the air in the space of dried and clean and puts cooling 20 hours; Again with mixer mixing on the sizing material 4 minutes; In mixing last minute, added vulcanization accelerator iso-cyanuric acid triallyl ester, vulcanizing agent cumyl peroxide successively at interval in 15 seconds; Mixingly sheet under the discharging is made a call to behind six triangle bags in mill on the mixing materials after evenly, in the space of dried and clean, continue to dry in the air behind the following sheet put 10 hours subsequent use.
It is subsequent use to prepare jacket rubber again, and step is following: raw material, CSM H40:20 part are prepared by following component and weight content in (1); Vulcanization accelerator dibenzothiazyl disulfide: 0.5 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.4 part; Activating agent magnesia: 1.2 parts; Activating agent polyethylene glycol: 1.5 parts; Age resistor nickel dibutyl dithiocarbamate: 0.3 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.15 part; Plasticizer phthalic acid dioctyl ester: 2.8 parts; Fire retardant antimony oxide: 1.2 parts; Plasticizer chlorinated paraffin-52: 0.8 part; Fire retardant magnesium hydroxide: 1.2 parts; Filler semi-reinforcing hydrocarbon black: 0.8 part; Reinforcing filler precipitated silica: 6.0 parts; Filler superfine talcum powder: 10 parts; (2) be on 80 ℃ the banbury mixing 3.5 minutes in temperature earlier with CSM H40 rubber; Add activating agent magnesia, activating agent polyethylene glycol, fire retardant antimony oxide, filler superfine talcum powder, plasticizer chlorinated paraffin-52, fire retardant magnesium hydroxide, plasticizer phthalic acid dioctyl ester, filler semi-reinforcing hydrocarbon black and reinforcing filler precipitated silica then successively on banbury mixing 5 minutes; On banbury, add age resistor 4 then successively; 4 '-two (α; α-Er Jiajibianji) diphenylamines, vulcanization accelerator dibenzothiazyl disulfide, age resistor nickel dibutyl dithiocarbamate and vulcanization accelerator six sulfuration di-penta methylene thiurams; Formed mixing materials in mixing again 50 seconds; The temperature of said mixing materials is controlled at 100 ℃ and move to and approach logical 5 heat radiations in the mill, in mill, turns over 8 triangle bags simultaneously, it is 9 minutes that whole in mill rolled the material time; Then through the tri-roll press machine slice, institute's slice was fast reduced to 35 ℃ with temperature through chill roll in 18 minutes, in the space of dried and clean, continue to dry in the air then put 11 hours subsequent use.
The step of making cable is following: be that the tinned copper wire of 0.3mm passes with the speed of 4.5m/s in the sealing glue of fusion with filament diameter earlier, make its surperficial thorough impregnation fluid sealant; Again multifilament is twisted into strand with 9 times lay ratio, the multiply strand is again according to being twisted into twisted copper conductors 1 with the stranded opposite direction of monofilament again with 14 times lay ratio; Twisted copper conductors 1 is passed with the speed of 35m/min in the sealing glue of fusion; Extrude conductor sealant layer 2 and electro-insulating rubber layer 3 simultaneously in twisted copper conductors 1 periphery then, conductor sealant layer 2 is interior, and electro-insulating rubber layer 3 outside; The periphery of electro-insulating rubber layer 3 is woven with aramid fiber silk reinforced layer 4 and constitutes the insulation heart yearn; Aramid fiber silk reinforced layer 4 is that the aramid fiber silk braiding of 0.18mm forms by diameter, and the hot strength of aramid fiber silk is 3500MPa, and modulus of elasticity is 150GPa; Angle of weave is 40 °, and percentage of braiding coverage is 40%; Place, the slit filling coefficient of expansion between each insulation heart yearn is 1.15 neoprene packing 5; Be 19 times with lay ratio then and be twisted into cable core; Then extrude sealant layer 6 and armour formula inner sheath rubber layer 7 in the cable core simultaneously in the cable core periphery; Sealant layer 6 is interior in the cable core, and inner sheath rubber layer 7 outside; Then use the tinned copper wire braiding armouring screen 8 of diameter as 0.3mm in the periphery of inner sheath rubber layer 7, angle of weave is 50 °, and percentage of braiding coverage is 90%; Periphery at armouring screen 8 extrudes cable core external seal glue-line 9 and armour formula oversheath rubber layer 10 simultaneously then, and cable core external seal glue-line 9 is interior, and oversheath rubber layer 10 outside.
80 ℃ of the head temperatures of rubber extruding machine when electro-insulating rubber is extruded, body temperature is 75 ℃, and the steam pressure of curing tube is 0.55MPa, and the rubber extruding machine type of cooling is water cooling.
Body temperature when jacket rubber is extruded is 65 ℃, and head temperature is 60 ℃, and the extruder temperature type of cooling of rubber extruding machine adopts water cooling, and extruding the back, to adopt pressure be that the pressure of 0.7MPa vulcanizes, and goes out linear velocity and be about 11m/min, and extruding thickness is 2.0mm.
Embodiment three
The preparation electro-insulating rubber is subsequent use earlier, and step is following: raw material is prepared by following component and weight content in (1): ethylene propylene diene rubber K21:15 part; Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.6 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.3 part; Age resistor 2 mercapto benzimidazole: 0.9 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.3 part; Plasticizer paraffin oil: 2.0 parts; Plasticizer chlorinated paraffin-52: 2 parts; Plasticizer microcrystalline wax: 1.0 parts; Activating agent zinc oxide: 2.0 parts; Activating agent stearic acid: 0.5 part; Filler superfine talcum powder: 11 parts; Reinforcing filler fume colloidal silica: 1.5 parts; Reinforcing filler calcinated argil: 9 parts; (2) be mixing until evenly on 75 ℃ the banbury in temperature earlier with ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M rubber; Add age resistor 2 mercapto benzimidazole, age resistor 2 then successively; 2; 4-trimethyl-1; 2-dihyaroquinoline condensate, plasticizer chlorinated paraffin-52, plasticizer paraffin oil, plasticizer microcrystalline wax, activating agent zinc oxide, activating agent stearic acid, reinforcing filler fume colloidal silica, reinforcing filler calcinated argil and filler superfine talcum powder on banbury mixing 16 minutes; Mixing even back is gone up mill and is played the triangle bag eight times, adopts slice behind 20 orders+40 orders+60 orders+80 orders, four metafiltration nets filter rubber then, dries in the air in the space of dried and clean and puts cooling 24 hours; Again with mixer mixing on the sizing material 5 minutes; In mixing last minute, added vulcanization accelerator iso-cyanuric acid triallyl ester, vulcanizing agent cumyl peroxide successively at interval in 20 seconds; Mixingly sheet under the discharging is made a call to behind six triangle bags in mill on the mixing materials after evenly, in the space of dried and clean, continue to dry in the air behind the following sheet put 12 hours subsequent use.
It is subsequent use to prepare jacket rubber again, and step is following: raw material, CSM H40:20 part are prepared by following component and weight content in (1); Vulcanization accelerator dibenzothiazyl disulfide: 0.6 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.5 part; Activating agent magnesia: 1.5 parts; Activating agent polyethylene glycol: 2.0 parts; Age resistor nickel dibutyl dithiocarbamate: 0.4 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.2 part; Plasticizer phthalic acid dioctyl ester: 3.0 parts; Fire retardant antimony oxide: 1.5 parts; Plasticizer chlorinated paraffin-52: 1 part; Fire retardant magnesium hydroxide: 1.5 parts; Filler semi-reinforcing hydrocarbon black: 1 part; Reinforcing filler precipitated silica: 6.5 parts; Filler superfine talcum powder: 12 parts; (2) be on 85 ℃ the banbury mixing 4 minutes in temperature earlier with CSM H40 rubber; Add activating agent magnesia, activating agent polyethylene glycol, fire retardant antimony oxide, filler superfine talcum powder, plasticizer chlorinated paraffin-52, fire retardant magnesium hydroxide, plasticizer phthalic acid dioctyl ester, filler semi-reinforcing hydrocarbon black and reinforcing filler precipitated silica then successively on banbury mixing 6 minutes; On banbury, add age resistor 4 then successively; 4 '-two (α; α-Er Jiajibianji) diphenylamines, vulcanization accelerator dibenzothiazyl disulfide, age resistor nickel dibutyl dithiocarbamate and vulcanization accelerator six sulfuration di-penta methylene thiurams; Formed mixing materials in mixing again 60 seconds; The temperature of said mixing materials is controlled at 110 ℃ and move to and approach logical 6 heat radiations in the mill, in mill, turns over 8 triangle bags simultaneously, it is 10 minutes that whole in mill rolled the material time; Then through the tri-roll press machine slice, institute's slice was fast reduced to 30 ℃ with temperature through chill roll in 20 minutes, in the space of dried and clean, continue to dry in the air then put 13 hours subsequent use.
The step of making cable is following: be that the tinned copper wire of 0.4mm passes with the speed of 5m/s in the sealing glue of fusion with filament diameter earlier, make its surperficial thorough impregnation fluid sealant; Again multifilament is twisted into strand with 10 times lay ratio, the multiply strand is again according to being twisted into twisted copper conductors 1 with the stranded opposite direction of monofilament again with 16 times lay ratio; Twisted copper conductors 1 is passed with the speed of 40m/min in the sealing glue of fusion; Extrude conductor sealant layer 2 and electro-insulating rubber layer 3 simultaneously in twisted copper conductors 1 periphery then, conductor sealant layer 2 is interior, and electro-insulating rubber layer 3 outside; The periphery of electro-insulating rubber layer 3 is woven with aramid fiber silk reinforced layer 4 and constitutes the insulation heart yearn; Aramid fiber silk reinforced layer 4 is that the aramid fiber silk braiding of 0.2mm forms by diameter, and the hot strength of aramid fiber silk is 4000MPa, and modulus of elasticity is 200GPa; Angle of weave is 50 °, and percentage of braiding coverage is 45%; Place, the slit filling coefficient of expansion between each insulation heart yearn is 1.2 neoprene packing 5; Be 20 times with lay ratio then and be twisted into cable core; Then extrude sealant layer 6 and armour formula inner sheath rubber layer 7 in the cable core simultaneously in the cable core periphery; Sealant layer 6 is interior in the cable core, and inner sheath rubber layer 7 outside; Then use the tinned copper wire braiding armouring screen 8 of diameter as 0.3mm in the periphery of inner sheath rubber layer 7, angle of weave is 60 °, and percentage of braiding coverage is 92%; Periphery at armouring screen 8 extrudes cable core external seal glue-line 9 and armour formula oversheath rubber layer 10 simultaneously then, and cable core external seal glue-line 9 is interior, and oversheath rubber layer 10 outside.
85 ℃ of the head temperatures of rubber extruding machine when electro-insulating rubber is extruded; Body temperature is 80 ℃; The steam pressure of curing tube is 0.6MPa, and the rubber extruding machine type of cooling is water cooling.
Body temperature when jacket rubber is extruded is 70 ℃, and head temperature is 65 ℃, and the extruder temperature type of cooling of rubber extruding machine adopts water cooling, and extruding the back, to adopt pressure be that the pressure of 0.8MPa vulcanizes, and goes out linear velocity and be about 12m/min, and extruding thickness is 2.2mm.
To electro-insulating rubber among the embodiment one to embodiment three aging before measuring mechanical property result such as table 1:
Table 1
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Tensile strength | N/mm2 | ≥4.8 | 7.5 | 7.3 | 6.7 |
| Elongation at break | % | ≥200 | 350 | 295 | 420 |
To measuring mechanical property result such as the table 2 behind the electro-insulating rubber oven ageing among the embodiment one to embodiment three, aging condition: 135 ± 2 ℃ of temperature, time: 168h.
Table 2
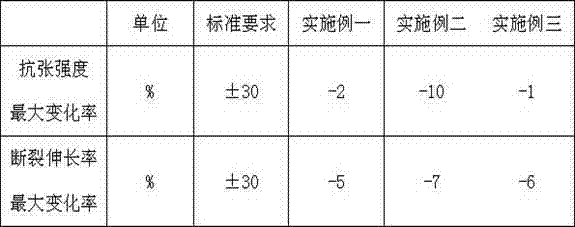
To measuring mechanical property result such as the table 3 behind the electro-insulating rubber air bomb aging among the embodiment one to embodiment three, aging condition: 127 ± 1 ℃ of temperature, time 40h, pressure 56 N/mm2.
Table 3
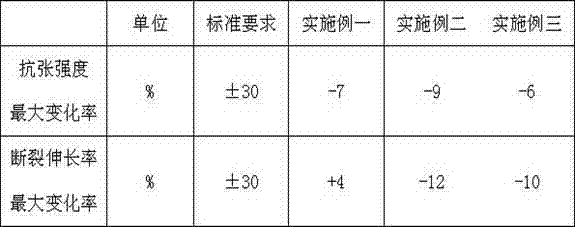
To the measuring mechanical property result such as the table 4 of the hot elongation test of electro-insulating rubber among the embodiment one to embodiment three, experimental condition: 250 ± 3 ℃ of treatment temperatures, duration 15 min, mechanical stress 20 N/cm2.
Table 4
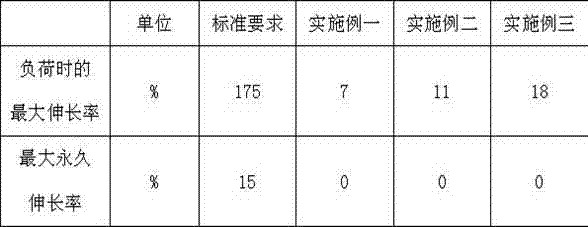
As shown in table 5 to the insulation resistance of electro-insulating rubber among the embodiment one to embodiment three (20 ℃ time) test result.
Table 5
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Insulation resistance (20 ℃) | MΩ·km | ≥1100 | 3670 | 3450 | 3620 |
To ac capacitor increment rate test result such as table 6 behind 50 ℃ of water of electro-insulating rubber immersion among the embodiment one to embodiment three.In the table numerical values recorded be respectively the 14th day with the 1st day, the 7th day difference.
Table 6
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| 14-1(d) | % | ≤15 | 2.7 | 4.2 | 3.8 |
| 14-7(d) | % | ≤5 | 0.5 | 1.7 | 0.6 |
To additional ageing test result of finished cable among the embodiment one to embodiment three such as table 7, aging condition: 95 ± 2 ℃ of temperature, time 168h.
Table 7
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| The maximum rate of change of tensile strength | % | ±30 | -5 | -10 | -8 |
| The maximum rate of change of elongation at break | % | ±30 | -7 | -9 | -3 |
To finished cable ozone resistance test result such as table 8 among the embodiment one to embodiment three, experimental condition: 25 ± 2 ℃ of temperature, time 30h, ozone concentration 0.025~0.030%.
Table 8
| ? | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Ozone resistance test | The surface does not have cracking | There is not cracking | There is not cracking | There is not cracking |
To jacket rubber among the embodiment one to embodiment three aging before measuring mechanical property result such as table 9:
Table 9
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Tensile strength | N/mm2 | ≥10 | 16.0 | 14.5 | 16.5 |
| Elongation at break | % | ≥250 | 390 | 410 | 330 |
To measuring mechanical property result such as the table 10 behind the jacket rubber oven ageing among the embodiment one to embodiment three, aging condition: 100 ± 2 ℃ of temperature, time: 168h.
Table 10
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Tensile strength is minimum percent before aging | % | 70 | 96 | 87 | 106 |
| Elongation at break is minimum percent before aging | % | 60 | 99 | 92 | 88 |
To carrying out measuring mechanical property, test result such as table 11 behind the jacket rubber immersion IRM902# oil among the embodiment one to embodiment three.Test condition: 100 ± 2 ℃ of temperature, time 24h.
Table 11
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Tensile strength is a minimum percent before the immersion oil | % | 60 | 94 | 79 | 93 |
| Elongation at break is a minimum percent before the immersion oil | % | 60 | 103 | 81 | 80 |
To jacket rubber ozone resistance test result such as table 12 among the embodiment one to embodiment three, experimental condition: 25 ± 2 ℃ of temperature, time 24h, ozone concentration 0.025~0.030%.
Table 12
| ? | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Ozone resistance test | The surface does not have cracking | There is not cracking | There is not cracking | There is not cracking |
To radially watertightness performance, direction waterproof performance test of finished cable among the embodiment one to embodiment three, result such as table 13:
Table 13
| Experimental condition | Standard-required | Embodiment one | Embodiment two | Embodiment three | |
| Watertightness performance radially | 7MPa,2h | The termination does not have infiltration | There is not infiltration | There is not infiltration | There is not infiltration |
| Watertightness performance radially | 3 MPa, withstand voltage 7kV, 5min | Do not puncture | Do not puncture | Do not puncture | Do not puncture |
| The direction waterproof performance | 7MPa,6h | The termination does not have infiltration, and assembly is no more than 6.4mm with respect to the displacement of sheath | There is not infiltration; Displacement 0.4mm | There is not infiltration; Non-displacement | There is not infiltration; Displacement 0.6mm |
| The direction waterproof performance | 5MPa,24h | The termination does not have infiltration, and assembly is no more than 6.4mm with respect to the displacement of sheath | There is not infiltration; Non-displacement | There is not infiltration; Non-displacement | There is not infiltration; Non-displacement |
| Vertical air-tightness | 0.3MPa,20min | Assembly is with respect to the non-displacement of sheath | Non-displacement | Non-displacement | Non-displacement |
Finished cable among the embodiment one to embodiment three was soaked 30 days in 40 ± 1 ℃ saliferous (NaCl) concentration is the seawater of 40g/L, and insulation resistance is seen table 14; Immerse seawater and bear after 14 days that withstand voltage (7kV, 5min), result of the test is also seen table 14.
Table 14
| ? | Unit | Standard-required | Embodiment one | Embodiment two | Embodiment three |
| Insulation resistance (is to soak 30 days in the seawater of 40g/L in 40 ± 1 ℃ saliferous (NaCl) concentration) | MΩ·km | ≥100 | 370 | 340 | 360 |
| Immerse seawater bear after 14 days withstand voltage (7kV, 5min) | ? | Do not puncture | Do not puncture | Do not puncture | Do not puncture |
Ethylene propylene diene rubber K21 can select the satisfied illustrious and influential science and trade Co., Ltd in Beijing for use or go up sea blue trade Co., Ltd product, and ethylene propylene diene rubber 4045M can select the product of Mitsui chemicals Co., Ltd. for use.CSM H40 can select du pont company, the satisfied illustrious and influential science and trade Co., Ltd in Beijing for use or go up sea blue trade Co., Ltd product.
The vulcanizing agent cumyl peroxide is claimed vulcanizing agent DCP again, and the vulcanization accelerator iso-cyanuric acid triallyl ester is claimed vulcanization accelerator TAIC again, can select for use permanent promise Chemical Industry Science Co., Ltd in Yantai or Shanghai Fang Rui to reach chemicals Co., Ltd product.The vulcanization accelerator dibenzothiazyl disulfide is claimed vulcanizing agent DM again, molecular formula: C14H8N2S4, select the top grade article that meet in " GB/T 11408-2003 accelerator DM " for use.Vulcanization accelerator six sulfuration di-penta methylene thiurams are claimed accelerator D PTT again, and molecular formula C12H20N2S6 can select chemical Co., Ltd of Hua Xing (Suqian) or Hebi City Rong Xin auxiliary agent Co., Ltd product for use.
The age resistor 2 mercapto benzimidazole is claimed antioxidant MB again, age resistor 2,2, and 4-trimethyl-1,2-dihyaroquinoline condensate is claimed anti-aging agent RD again, can select Shanghai rubber chemicals Co., Ltd., Factory or Qingdao special promise commerce and trade Co., Ltd product for use.
The age resistor nickel dibutyl dithiocarbamate can select for use Wuhan City Ford Fine Chemical Co., Ltd or Shanghai nation to become the product of chemical industry Co., Ltd.
Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines is the product that antioxidant H S-911 can select Huangyan, Zhejiang China star laboratory, the chemical Co., Ltd of Hua Xing (Suqian) or the prosperous luxuriant Chemical Industry Science Co., Ltd in Shijiazhuang for use.
Paraffin oil can be selected the product of Hengshui, Hebei Sheng Kang chemical industry Co., Ltd or Hengshui, Hebei Supreme Being hundred million petrochemical industry Co., Ltds for use; Chlorinated paraffin-52 requires to meet the standard in " the chemical industry standard HG2092-1991 of People's Republic of China (PRC) chlorinated paraffin-52 ", and microcrystalline wax can be selected the product of China Petroleum & Chemical Corporation Henan Oil Field Branch Nanyang Paraffin Fine Chemical Plant or Shanghai Tai Er petrochemical industry Science and Technology Ltd. for use.
Activating agent zinc oxide can be selected the product of Henan zincaluminite chemical industry Co., Ltd, the grand auspicious zinc industry Co., Ltd in Shandong or Dongying Feng He chemical industry Co., Ltd for use, carries out the standard in " GB/T3185-1992 zinc oxide (activity) ".Activating agent stearic acid formal name used at school: octadecanoid acid, molecular formula CH3 (CH2) 16COOH carries out the standard in " GB/T 9103-1988 industry stearic acid ".
Activating agent magnesia can select for use Weifang Hai Lilong magnesium industry Co., Ltd or Xingtai City magnesium to deify the product of worker Co., Ltd, and the activating agent polyethylene glycol can be selected the product of Jiangsu Jia Feng chemistry limited company or the chemical industry that circles in the air (Zhangjiagang) Co., Ltd for use.
Carbon black can be selected the product of Changzhou cloud moon chemical industry Co., Ltd or Dongguan Yu Chang chemical industry Co., Ltd for use.Precipitated silica can be selected the product of precious specialization worker Co., Ltd in Shouguang City or Dongying City friendship maritime works trade Co., Ltd for use.All the other white carbons can be selected the product of Guangzhou Science and Technology Ji Sheng Industrial Co or the inferior rubber and plastic auxiliary agent of Shanghai Xiang Co., Ltd for use.The filler superfine talcum powder is selected for use and is met the product of stipulating in " GB 15342-1994 talcum powder " standard.The reinforcing filler calcinated argil can be selected the product of Shanghai, river, Shanghai titanium white heavy chemicals Co., Ltd or Shijiazhuang Tourmaline mineral products Co., Ltd for use.
The plasticizer phthalic acid dioctyl ester is a plasticizer DOP, selects the product that meets " GB/T 11406-2001 industry dioctyl phthalate " standard for use.
The fire retardant antimony oxide can be selected the product of Anhua, Hunan Province China space antimony industry Co., Ltd or Changzhou money river chemical industry Co., Ltd for use.
The present invention is raw materials used, except that above producer, all can select other satisfactory like product on the market for use.
Except that the foregoing description, the present invention can also have other execution modes.All employings are equal to the technical scheme of replacement or equivalent transformation formation, all drop on the protection range of requirement of the present invention.
Claims (9)
1. a naval vessel is with strengthening tension shield type direction waterproof degaussing cable; It is characterized in that; The stranded twisted copper conductors that becomes behind the many tinned copper wire dipping fluid sealants; Said twisted copper conductors periphery is impregnated with the conductor sealant layer, and the periphery of said conductor sealant layer is extruded with the electro-insulating rubber layer, and the periphery of said electro-insulating rubber layer is woven with aramid fiber silk reinforced layer and constitutes the insulation heart yearn; Place, slit between each said insulation heart yearn is filled with the neoprene packing and many said insulation heart yearn integral body are twisted into cable core; The periphery of said cable core is extruded with sealant layer in the cable core, and the periphery of sealant layer is extruded with the inner sheath rubber layer in the said cable core, and the periphery of said inner sheath rubber layer is woven with the armouring screen; The periphery of said armouring screen is extruded with cable core external seal glue-line, and the periphery of said cable core external seal glue-line is extruded with the oversheath rubber layer.
2. naval vessel according to claim 1 is with strengthening tension shield type direction waterproof degaussing cable; It is characterized in that; The filament diameter of said twisted copper conductors is 0.2~0.4mm; Lay ratio with 8~10 times is twisted into strand, and said strand is twisted into said twisted copper conductors according to the direction opposite with former bundle strand with 12~16 times lay ratio more again; The stranded lay ratio of said cable core is 18~20 times; The coefficient of expansion of said neoprene packing is 1.1~1.2; Said aramid fiber silk reinforced layer is that the aramid fiber silk braiding of 0.15~0.2mm forms by diameter; The hot strength of said aramid fiber silk is 3000MPa~4000MPa; Modulus of elasticity is 100GPa~200GPa, and angle of weave is between 30 °~50 °, and percentage of braiding coverage is 30%~45%; Said armouring screen is that the tinned copper wire braiding of 0.3mm forms by diameter, and angle of weave is 40 °~60 °, and percentage of braiding coverage is 88%~92%.
3. naval vessel according to claim 1 is characterized in that the raw material components and the weight content of said electro-insulating rubber layer are following: ethylene propylene diene rubber K21:15 part with strengthening tension shield type direction waterproof degaussing cable; Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.5~0.6 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.2~0.3 part; Age resistor 2 mercapto benzimidazole: 0.7~0.9 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.2~0.3 part; Plasticizer paraffin oil: 1.0~2.0 parts; Plasticizer chlorinated paraffin-52: 1~2 part; Plasticizer microcrystalline wax: 0.5~1.0 part; Activating agent zinc oxide: 1.0~2.0 parts; Activating agent stearic acid: 0.3~0.5 part; Filler superfine talcum powder: 8~11 parts; Reinforcing filler fume colloidal silica: 1.0~1.5 parts; Reinforcing filler calcinated argil: 7~9 parts.
4. naval vessel according to claim 1 is characterized in that the raw material components and the weight content of said inner sheath rubber layer and oversheath rubber layer are following: CSM H40:20 part with strengthening tension shield type direction waterproof degaussing cable; Vulcanization accelerator dibenzothiazyl disulfide: 0.4~0.6 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.3~0.5 part; Activating agent magnesia: 1.0~1.5 parts; Activating agent polyethylene glycol: 1.0~2.0 parts; Age resistor nickel dibutyl dithiocarbamate: 0.2~0.4 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.1~0.2 part; Plasticizer phthalic acid dioctyl ester: 2.5~3.0 parts; Fire retardant antimony oxide: 1~1.5 part; Plasticizer chlorinated paraffin-52: 0.5~1 part; Fire retardant magnesium hydroxide: 1~1.5 part; Filler semi-reinforcing hydrocarbon black: 0.5~1 part; Reinforcing filler precipitated silica: 5.5~6.5 parts; Filler superfine talcum powder: 8~12 parts.
5. a naval vessel is with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable; It is characterized in that; May further comprise the steps: be that the tinned copper wire of 0.2~0.4mm passes with the speed of 4~5m/s in the sealing glue of fusion earlier, make its surperficial thorough impregnation fluid sealant filament diameter; Again multifilament is twisted into strand with 8~10 times lay ratio, the multiply strand is again according to being twisted into twisted copper conductors with the stranded opposite direction of monofilament again with 12~16 times lay ratio; Said twisted copper conductors is passed with the speed of 30~40m/min in the sealing glue of fusion, extrudes conductor sealant layer and electro-insulating rubber layer simultaneously in the twisted copper conductors periphery then, and said conductor sealant layer is interior, and said electro-insulating rubber layer outside; The periphery braiding aramid fiber silk reinforced layer of said electro-insulating rubber layer constitutes the insulation heart yearn; Place, the slit filling coefficient of expansion between each said insulation heart yearn is 1.1~1.2 neoprene packing; Be 18~20 times with lay ratio then and be twisted into cable core; Then extrude sealant layer and inner sheath rubber layer in the cable core simultaneously in the cable core periphery; Sealant layer is interior in the said cable core, and said inner sheath rubber layer outside; Then at the periphery of inner sheath rubber layer braiding armouring screen, extrude cable core external seal glue-line and oversheath rubber layer simultaneously in the periphery of armouring screen, cable core external seal glue-line is interior, and the oversheath rubber layer is outside.
6. naval vessel according to claim 5 is with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable; It is characterized in that; The preparation method of the electro-insulating rubber of said electro-insulating rubber layer is following: raw material, ethylene propylene diene rubber K21:15 part are prepared by following component and weight content in (1); Ethylene propylene diene rubber 4045M:5 part; Vulcanizing agent cumyl peroxide: 0.5~0.6 part; Vulcanization accelerator iso-cyanuric acid triallyl ester: 0.2~0.3 part; Age resistor 2 mercapto benzimidazole: 0.7~0.9 part; Age resistor 2,2,4-trimethyl-1,2-dihyaroquinoline condensate: 0.2~0.3 part; Plasticizer paraffin oil: 1.0~2.0 parts; Plasticizer chlorinated paraffin-52: 1~2 part; Plasticizer microcrystalline wax: 0.5~1.0 part; Activating agent zinc oxide: 1.0~2.0 parts; Activating agent stearic acid: 0.3~0.5 part; Filler superfine talcum powder: 8~11 parts; Reinforcing filler fume colloidal silica: 1.0~1.5 parts; Reinforcing filler calcinated argil: 7~9 parts; (2) be mixing until evenly on 65 ℃~75 ℃ the banbury in temperature earlier with ethylene propylene diene rubber K21 and ethylene propylene diene rubber 4045M rubber; Add age resistor 2 mercapto benzimidazole, age resistor 2 then successively; 2; 4-trimethyl-1; 2-dihyaroquinoline condensate, plasticizer chlorinated paraffin-52, plasticizer paraffin oil, plasticizer microcrystalline wax, activating agent zinc oxide, activating agent stearic acid, reinforcing filler fume colloidal silica, reinforcing filler calcinated argil and filler superfine talcum powder on banbury mixing 14~16 minutes; Mixing even back is gone up mill and is played the triangle bag eight times, adopts slice behind 20 orders+40 orders+60 orders+80 orders, four metafiltration nets filter rubber then, dries in the air in the space of dried and clean and puts cooling 18~24 hours; Again with mixer mixing on the sizing material 3~5 minutes; In mixing last minute, added vulcanization accelerator iso-cyanuric acid triallyl ester, vulcanizing agent cumyl peroxide successively at interval in 10~20 seconds; Mixingly sheet under the discharging is made a call to behind six triangle bags in mill on the mixing materials after evenly, in the space of dried and clean, continue to dry in the air behind the following sheet put 8~12 hours subsequent use.
7. naval vessel according to claim 6 is characterized in that with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable, 80 ℃ ± 5 ℃ of the head temperatures of rubber extruding machine when said electro-insulating rubber is extruded; Body temperature is 75 ℃ ± 5 ℃; The steam pressure of curing tube is 0.5~0.6MPa, and the rubber extruding machine type of cooling is water cooling.
8. naval vessel according to claim 5 is with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable; It is characterized in that; The preparation method of the jacket rubber of said inner sheath rubber layer and oversheath rubber layer is following: raw material, CSM H40:20 part are prepared by following component and weight content in (1); Vulcanization accelerator dibenzothiazyl disulfide: 0.4~0.6 part; Vulcanization accelerator six sulfuration di-penta methylene thiurams: 0.3~0.5 part; Activating agent magnesia: 1.0~1.5 parts; Activating agent polyethylene glycol: 1.0~2.0 parts; Age resistor nickel dibutyl dithiocarbamate: 0.2~0.4 part; Age resistor 4,4 '-two (α, α-Er Jiajibianji) diphenylamines: 0.1~0.2 part; Plasticizer phthalic acid dioctyl ester: 2.5~3.0 parts; Fire retardant antimony oxide: 1~1.5 part; Plasticizer chlorinated paraffin-52: 0.5~1 part; Fire retardant magnesium hydroxide: 1~1.5 part; Filler semi-reinforcing hydrocarbon black: 0.5~1 part; Reinforcing filler precipitated silica: 5.5~6.5 parts; Filler superfine talcum powder: 8~12 parts; (2) be on 75 ℃~85 ℃ the banbury mixing 3~4 minutes in temperature earlier with CSM H40 rubber; Add activating agent magnesia, activating agent polyethylene glycol, fire retardant antimony oxide, filler superfine talcum powder, plasticizer chlorinated paraffin-52, fire retardant magnesium hydroxide, plasticizer phthalic acid dioctyl ester, filler semi-reinforcing hydrocarbon black and reinforcing filler precipitated silica then successively on banbury mixing 4~6 minutes; Then on banbury, add age resistor 4 successively; 4 '-two (α; α-Er Jiajibianji) diphenylamines, vulcanization accelerator dibenzothiazyl disulfide, age resistor nickel dibutyl dithiocarbamate and vulcanization accelerator six sulfuration di-penta methylene thiurams; Formed mixing materials in mixing again 40~60 seconds; The temperature of said mixing materials is controlled at 90 ℃~110 ℃ and move to and approach logical 4~6 heat radiations in the mill, in mill, turns over 8 triangle bags simultaneously, it is 8~10 minutes that whole in mill rolled the material time; Then through the tri-roll press machine slice, institute's slice was fast reduced to 30 ℃~40 ℃ with temperature through chill roll in 15~20 minutes, and in the space of dried and clean, continuing to dry in the air then, it is subsequent use to put more than 10 hours.
9. naval vessel according to claim 8 is with the manufacturing approach that strengthens tension shield type direction waterproof degaussing cable; It is characterized in that the body temperature when said jacket rubber is extruded is 65 ± 5 ℃, head temperature is 60 ± 5 ℃; The extruder temperature type of cooling of rubber extruding machine adopts water cooling; Extruding the back, to adopt pressure be that the pressure of 0.6~0.8MPa vulcanizes, and goes out linear velocity and be about 10~12m/min, and extruding thickness is 1.8~2.2mm.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210203842.8A CN102737760B (en) | 2012-06-20 | 2012-06-20 | Reinforced tensile screening type vertical watertight degaussing cable for ship and manufacturing method thereof |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201210203842.8A CN102737760B (en) | 2012-06-20 | 2012-06-20 | Reinforced tensile screening type vertical watertight degaussing cable for ship and manufacturing method thereof |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| CN102737760A true CN102737760A (en) | 2012-10-17 |
| CN102737760B CN102737760B (en) | 2014-01-29 |
Family
ID=46993080
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201210203842.8A Expired - Fee Related CN102737760B (en) | 2012-06-20 | 2012-06-20 | Reinforced tensile screening type vertical watertight degaussing cable for ship and manufacturing method thereof |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN102737760B (en) |
Cited By (27)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102969063A (en) * | 2012-11-16 | 2013-03-13 | 江苏远洋东泽电缆股份有限公司 | High-temperature-resistant soft power cable for maritime oil and gas engineering and manufacturing method thereof |
| CN102982875A (en) * | 2012-11-28 | 2013-03-20 | 安徽埃克森科技集团有限公司 | Cable |
| CN103123830A (en) * | 2013-03-14 | 2013-05-29 | 南京科孚纳米技术有限公司 | Method for preparing graphene wire and cable |
| CN103680708A (en) * | 2013-12-20 | 2014-03-26 | 中天科技海缆有限公司 | Flexible positive buoyancy cable floating on water surface |
| CN103881252A (en) * | 2014-02-14 | 2014-06-25 | 安徽旺达铜业发展有限公司 | Waterproof rubber cable material for submersible motor and preparation method thereof |
| CN103903753A (en) * | 2014-03-05 | 2014-07-02 | 安徽神州缆业集团有限公司 | Armored insulating and shielding sheath cable used for petrochemical engineering |
| CN104143388A (en) * | 2014-07-11 | 2014-11-12 | 安徽宏源特种电缆集团有限公司 | Watertight tractive load-bearing control cable |
| CN104143390A (en) * | 2014-07-11 | 2014-11-12 | 安徽宏源特种电缆集团有限公司 | Deep water seal rubber sleeve cable and manufacturing process thereof |
| CN104318998A (en) * | 2014-10-21 | 2015-01-28 | 江苏中煤电缆有限公司 | Watertight degaussing cable |
| CN104761909A (en) * | 2015-04-02 | 2015-07-08 | 西安飞机工业(集团)亨通航空电子有限公司 | Preparation method of super-soft cable and external coating material of super-soft cable |
| CN104867538A (en) * | 2015-04-02 | 2015-08-26 | 西安飞机工业(集团)亨通航空电子有限公司 | Cable with extremely small bending radius and preparation method of externally coating material thereof |
| CN104867548A (en) * | 2014-02-26 | 2015-08-26 | 安徽江淮电缆集团有限公司 | Nickel conductor wire core cable with copper metal hose |
| CN105336415A (en) * | 2015-10-30 | 2016-02-17 | 江苏中煤电缆有限公司 | Double-sheath structured degaussing cable |
| CN105427937A (en) * | 2015-12-30 | 2016-03-23 | 合肥星辰电线电缆股份有限公司 | Ship-used watertight degaussing cable |
| CN105448429A (en) * | 2015-12-30 | 2016-03-30 | 合肥星辰电线电缆股份有限公司 | Production process of cable |
| CN105448400A (en) * | 2016-01-06 | 2016-03-30 | 四川金开特种电线电缆有限公司 | Deep seawater density exploration cable and production method therefor |
| CN105623111A (en) * | 2016-03-04 | 2016-06-01 | 王金武 | Anti-fatigue and anti-bending composite rubber cable sleeve |
| CN104751997B (en) * | 2013-12-25 | 2016-08-17 | 江苏亨通线缆科技有限公司 | High-frequency data transmission cable for maritime affairs |
| CN106977822A (en) * | 2017-03-31 | 2017-07-25 | 长乐巧通工业设计有限公司 | A kind of anti-aging CABLE MATERIALS and preparation method thereof |
| CN107603054A (en) * | 2017-07-29 | 2018-01-19 | 安徽蓝德集团股份有限公司 | A kind of preparation method of coal-winning machine shielding monitoring cable and its cable jacket |
| CN108109726A (en) * | 2017-12-01 | 2018-06-01 | 新宇电缆集团股份有限公司 | A kind of airport is with from ice melting electric cable |
| CN112164493A (en) * | 2020-09-29 | 2021-01-01 | 安徽华宇电缆集团有限公司 | Demagnetization cable for special fixed winding of underwater vehicle |
| CN112309622A (en) * | 2020-09-27 | 2021-02-02 | 新亚特电缆股份有限公司 | Degaussing cable for ship |
| CN112331382A (en) * | 2020-10-14 | 2021-02-05 | 南京信宁电缆有限公司 | Anti-interference capacitive cable and manufacturing method thereof |
| CN112382438A (en) * | 2020-10-23 | 2021-02-19 | 新亚特电缆股份有限公司 | Longitudinal watertight degaussing cable for ships |
| CN116864189A (en) * | 2023-08-01 | 2023-10-10 | 中天科技装备电缆有限公司 | Light monitoring cable and manufacturing method thereof |
| CN119296879A (en) * | 2024-12-13 | 2025-01-10 | 湖南华菱线缆股份有限公司 | A tensile and extrusion-resistant watertight cable and a preparation method thereof |
Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101789281A (en) * | 2009-11-13 | 2010-07-28 | 曹洪波 | Novel wind power cable |
| CN101834023A (en) * | 2010-04-23 | 2010-09-15 | 江苏远洋东泽电缆股份有限公司 | Zero-halogen longitudinal water sealed high-voltage cable for ships and warships and manufacture method thereof |
| CN201868131U (en) * | 2010-10-25 | 2011-06-15 | 常州船用电缆有限责任公司 | Reinforced flexible cable for warships |
| CN202694867U (en) * | 2012-06-20 | 2013-01-23 | 江苏远洋东泽电缆股份有限公司 | Strengthening tensile shielding type longitudinal watertight degaussing cable used for ships and warships |
-
2012
- 2012-06-20 CN CN201210203842.8A patent/CN102737760B/en not_active Expired - Fee Related
Patent Citations (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101789281A (en) * | 2009-11-13 | 2010-07-28 | 曹洪波 | Novel wind power cable |
| CN101834023A (en) * | 2010-04-23 | 2010-09-15 | 江苏远洋东泽电缆股份有限公司 | Zero-halogen longitudinal water sealed high-voltage cable for ships and warships and manufacture method thereof |
| CN201868131U (en) * | 2010-10-25 | 2011-06-15 | 常州船用电缆有限责任公司 | Reinforced flexible cable for warships |
| CN202694867U (en) * | 2012-06-20 | 2013-01-23 | 江苏远洋东泽电缆股份有限公司 | Strengthening tensile shielding type longitudinal watertight degaussing cable used for ships and warships |
Cited By (31)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102969063A (en) * | 2012-11-16 | 2013-03-13 | 江苏远洋东泽电缆股份有限公司 | High-temperature-resistant soft power cable for maritime oil and gas engineering and manufacturing method thereof |
| CN102969063B (en) * | 2012-11-16 | 2014-12-10 | 江苏远洋东泽电缆股份有限公司 | High-temperature-resistant soft power cable for maritime oil and gas engineering and manufacturing method thereof |
| CN102982875A (en) * | 2012-11-28 | 2013-03-20 | 安徽埃克森科技集团有限公司 | Cable |
| CN103123830A (en) * | 2013-03-14 | 2013-05-29 | 南京科孚纳米技术有限公司 | Method for preparing graphene wire and cable |
| CN103680708A (en) * | 2013-12-20 | 2014-03-26 | 中天科技海缆有限公司 | Flexible positive buoyancy cable floating on water surface |
| CN104751997B (en) * | 2013-12-25 | 2016-08-17 | 江苏亨通线缆科技有限公司 | High-frequency data transmission cable for maritime affairs |
| CN103881252A (en) * | 2014-02-14 | 2014-06-25 | 安徽旺达铜业发展有限公司 | Waterproof rubber cable material for submersible motor and preparation method thereof |
| CN104867548A (en) * | 2014-02-26 | 2015-08-26 | 安徽江淮电缆集团有限公司 | Nickel conductor wire core cable with copper metal hose |
| CN103903753A (en) * | 2014-03-05 | 2014-07-02 | 安徽神州缆业集团有限公司 | Armored insulating and shielding sheath cable used for petrochemical engineering |
| CN104143390B (en) * | 2014-07-11 | 2017-10-24 | 安徽宏源特种电缆集团有限公司 | A kind of manufacturing process of deep water sealing Plastic-sheathed Cable |
| CN104143388A (en) * | 2014-07-11 | 2014-11-12 | 安徽宏源特种电缆集团有限公司 | Watertight tractive load-bearing control cable |
| CN104143390A (en) * | 2014-07-11 | 2014-11-12 | 安徽宏源特种电缆集团有限公司 | Deep water seal rubber sleeve cable and manufacturing process thereof |
| CN104318998A (en) * | 2014-10-21 | 2015-01-28 | 江苏中煤电缆有限公司 | Watertight degaussing cable |
| CN104867538A (en) * | 2015-04-02 | 2015-08-26 | 西安飞机工业(集团)亨通航空电子有限公司 | Cable with extremely small bending radius and preparation method of externally coating material thereof |
| CN104867538B (en) * | 2015-04-02 | 2017-02-22 | 西安飞机工业(集团)亨通航空电子有限公司 | Cable with extremely small bending radius and preparation method of externally coating material thereof |
| CN104761909A (en) * | 2015-04-02 | 2015-07-08 | 西安飞机工业(集团)亨通航空电子有限公司 | Preparation method of super-soft cable and external coating material of super-soft cable |
| CN105336415A (en) * | 2015-10-30 | 2016-02-17 | 江苏中煤电缆有限公司 | Double-sheath structured degaussing cable |
| CN105427937A (en) * | 2015-12-30 | 2016-03-23 | 合肥星辰电线电缆股份有限公司 | Ship-used watertight degaussing cable |
| CN105448429A (en) * | 2015-12-30 | 2016-03-30 | 合肥星辰电线电缆股份有限公司 | Production process of cable |
| CN105448400A (en) * | 2016-01-06 | 2016-03-30 | 四川金开特种电线电缆有限公司 | Deep seawater density exploration cable and production method therefor |
| CN105623111A (en) * | 2016-03-04 | 2016-06-01 | 王金武 | Anti-fatigue and anti-bending composite rubber cable sleeve |
| CN106977822A (en) * | 2017-03-31 | 2017-07-25 | 长乐巧通工业设计有限公司 | A kind of anti-aging CABLE MATERIALS and preparation method thereof |
| CN107603054A (en) * | 2017-07-29 | 2018-01-19 | 安徽蓝德集团股份有限公司 | A kind of preparation method of coal-winning machine shielding monitoring cable and its cable jacket |
| CN108109726A (en) * | 2017-12-01 | 2018-06-01 | 新宇电缆集团股份有限公司 | A kind of airport is with from ice melting electric cable |
| CN112309622A (en) * | 2020-09-27 | 2021-02-02 | 新亚特电缆股份有限公司 | Degaussing cable for ship |
| CN112164493A (en) * | 2020-09-29 | 2021-01-01 | 安徽华宇电缆集团有限公司 | Demagnetization cable for special fixed winding of underwater vehicle |
| WO2022067934A1 (en) * | 2020-09-29 | 2022-04-07 | 安徽华宇电缆集团有限公司 | Special degaussing cable for fixed winding for underwater vehicle |
| CN112331382A (en) * | 2020-10-14 | 2021-02-05 | 南京信宁电缆有限公司 | Anti-interference capacitive cable and manufacturing method thereof |
| CN112382438A (en) * | 2020-10-23 | 2021-02-19 | 新亚特电缆股份有限公司 | Longitudinal watertight degaussing cable for ships |
| CN116864189A (en) * | 2023-08-01 | 2023-10-10 | 中天科技装备电缆有限公司 | Light monitoring cable and manufacturing method thereof |
| CN119296879A (en) * | 2024-12-13 | 2025-01-10 | 湖南华菱线缆股份有限公司 | A tensile and extrusion-resistant watertight cable and a preparation method thereof |
Also Published As
| Publication number | Publication date |
|---|---|
| CN102737760B (en) | 2014-01-29 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN102737760B (en) | Reinforced tensile screening type vertical watertight degaussing cable for ship and manufacturing method thereof | |
| CN102855982B (en) | Shielding longitudinal watertight degaussing cable and production method thereof for ships | |
| CN102751020B (en) | Longitudinal watertight degaussing cable for warship and manufacturing method thereof | |
| CN102751017B (en) | Strengthening tensile type longitudinal watertight degaussing cable for ships and warships and manufacturing method thereof | |
| CN102746589B (en) | Sheath rubber for longitudinal water-tight demagnetization cable used for ship, and manufacture method for sheath rubber | |
| CN102751013B (en) | Medium and high-voltage cable for moving petrochemical device and manufacturing method thereof | |
| CN102746587B (en) | Insulation rubber for longitudinal water-tight demagnetization cable used for ship, and manufacture method for insulation rubber | |
| CN102403067B (en) | Ethylene propylene rubber insulating fire-resistant medium-voltage power cable for marine engineering and method for producing same | |
| CN102969046A (en) | Whitening ultraviolet-proof double-shield instrument cable for ships and manufacturing method thereof | |
| CN102364591B (en) | Hard ethylene propylene rubber insulated control cable for ships and ocean and manufacturing method thereof | |
| CN103227008B (en) | The ocean wind-powered electricity generation Salt corrosion power cable of resistance to torsion and manufacture method thereof | |
| CN102751014B (en) | Highly flexible cable for drag chain and manufacturing method thereof | |
| CN103187126A (en) | Double-shielded instrument cable for flame-resistant and fire-resistant ship and manufacture method thereof | |
| CN102820083A (en) | High-flexibility shielding cable for drag chain and manufacturing method thereof | |
| CN102969056B (en) | Marine integral screening instrument cable capable of whitening and resisting ultraviolet and manufacturing method thereof | |
| CN108648849A (en) | High flexibility cross-linked polyolefin high-tension cable and preparation method thereof | |
| CN103187127B (en) | Salt corrosion and torsion resisting type shielding telecommunication cable used for ocean wind power and manufacturing method thereof | |
| CN102347107B (en) | Hard EPR (ethylene propylene rubber) insulated power cable for ships and oceans and manufacturing method thereof | |
| CN102176343B (en) | Cable for ship hydrophone equipment and manufacturing method thereof | |
| CN103971828A (en) | Marine water-tight cable | |
| CN102969048B (en) | Marine independent screening instrument cable capable of whitening and resisting ultraviolet and manufacturing method thereof | |
| CN102347099B (en) | EPR (ethylene propylene rubber) insulated cable for offshore oil device and manufacturing method thereof | |
| CN103227011A (en) | Salt corrosion-resistant and torsion-resistant integral shielding telecommunication cable for offshore wind power and manufacturing method of integral shielding telecommunication cable | |
| CN202694867U (en) | Strengthening tensile shielding type longitudinal watertight degaussing cable used for ships and warships | |
| CN103227007B (en) | The ocean wind-powered electricity generation Salt corrosion composite cable of resistance to torsion and manufacture method thereof |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C06 | Publication | ||
| PB01 | Publication | ||
| C10 | Entry into substantive examination | ||
| SE01 | Entry into force of request for substantive examination | ||
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| TR01 | Transfer of patent right |
Effective date of registration: 20191106 Address after: Room 107, building 3, No.118, Kangbao Road, ganyao Town, Jiashan County, Jiaxing City, Zhejiang Province Patentee after: Jiaxing Junhong Optical Co., Ltd Address before: 225129 Jiangsu city of Yangzhou province Guazhou town Hanjiang District Stone Road No. 2 Patentee before: Jiangsu Yuanyang Dongze Cable Co., Ltd. |
|
| TR01 | Transfer of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20140129 Termination date: 20210620 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |