EP4227229B1 - High-speed double-track blister pillow packing and cartoning packing integrated machine - Google Patents
High-speed double-track blister pillow packing and cartoning packing integrated machine Download PDFInfo
- Publication number
- EP4227229B1 EP4227229B1 EP22850634.1A EP22850634A EP4227229B1 EP 4227229 B1 EP4227229 B1 EP 4227229B1 EP 22850634 A EP22850634 A EP 22850634A EP 4227229 B1 EP4227229 B1 EP 4227229B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- grid
- conveyor device
- pillow
- cartoning
- grid conveyor
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images

Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/10—Feeding, e.g. conveying, single articles
- B65B35/24—Feeding, e.g. conveying, single articles by endless belts or chains
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/10—Feeding, e.g. conveying, single articles
- B65B35/16—Feeding, e.g. conveying, single articles by grippers
- B65B35/18—Feeding, e.g. conveying, single articles by grippers by suction-operated grippers
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B35/00—Supplying, feeding, arranging or orientating articles to be packaged
- B65B35/30—Arranging and feeding articles in groups
- B65B35/44—Arranging and feeding articles in groups by endless belts or chains
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B5/00—Packaging individual articles in containers or receptacles, e.g. bags, sacks, boxes, cartons, cans, jars
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B65/00—Details peculiar to packaging machines and not otherwise provided for; Arrangements of such details
- B65B65/003—Packaging lines, e.g. general layout
- B65B65/006—Multiple parallel packaging lines
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B9/00—Enclosing successive articles, or quantities of material, e.g. liquids or semiliquids, in flat, folded, or tubular webs of flexible sheet material; Subdividing filled flexible tubes to form packages
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65B—MACHINES, APPARATUS OR DEVICES FOR, OR METHODS OF, PACKAGING ARTICLES OR MATERIALS; UNPACKING
- B65B2220/00—Specific aspects of the packaging operation
- B65B2220/16—Packaging contents into primary and secondary packaging
- B65B2220/18—Packaging contents into primary and secondary packaging the primary packaging being bags the subsequent secondary packaging being rigid containers, e.g. cardboard box
Definitions
- the present disclosure relates to the field of pharmaceutical card packaging machines, particularly to a machine for packaging blister cards.
- blisters or blister cards In modern pharmaceutical packaging, a more flexible packaging solution for pharmaceutical blister cards is desired by pharmaceutical companies.
- pharmaceutical blister cards referred to as blisters or blister cards
- blisters or blister cards not only are cartoned (e.g., the pharmaceutical blister cards are directly packaged into cartons), but also are packaged into pillow bags to be placed into cartons.
- different packaging devices are used to provide perform different packaging manners, or the pharmaceutical cards are preliminarily distributed to a rear packaging device by a conveyor belt. This increases the equipment purchasing cost of the pharmaceutical companies and requires larger equipment space, higher mounting costs, and higher equipment operation and maintenance costs. Therefore, the prior art can hardly meet the demand of modern pharmaceutical packaging for flexibility in the new era.
- the Chinese Patent Application Publication CN 206 871 414 U discloses a high-speed double-line blister and pillow bag cartoning integrated machine, comprising a blister packaging machine, a pillow-type packaging machine, and a cartoning machine, wherein the blister packaging machine is connected to a discharging grid conveyor device for conveyance.
- a blister card transfer device is also included for transferring blister cards on the discharging grid conveyor device to a pillow bag conveyor chain device or a transiting grid conveyor device.
- the present disclosure provides a high-speed double-line blister and pillow bag cartoning integrated machine, which not only can directly carton the blisters but can also package the blisters into the pillow bags for cartoning.
- a high-speed double-line blister and pillow bag cartoning integrated machine includes a blister packaging machine, a pillow-type packaging machine, and a cartoning machine.
- the blister packaging machine is connected to a discharging grid conveyor device for conveyance.
- a pillow bag conveyor chain device is provided side by side at one side of the discharging grid conveyor device.
- the pillow bag conveyor chain device is connected to the pillow-type packaging machine for conveyance.
- An output end of the pillow-type packaging machine is connected to a pillow bag grid conveyor device for conveyance.
- One side of the pillow bag grid conveyor device is provided with a cartoning conveyor chain device, and the cartoning conveyor chain device is connected to the cartoning machine for conveyance.
- the other side of the discharging grid conveyor device is provided with a transiting grid conveyor device.
- the transiting grid conveyor device extends to one side of the cartoning conveyor chain device, and the cartoning conveyor chain device is located between the transiting grid conveyor device and the pillow bag grid conveyor device.
- a blister card transfer device for transferring blister cards on the discharging grid conveyor device to the pillow bag conveyor chain device or the transiting grid conveyor device is provided on the discharging grid conveyor device, and the blister card transfer device is provided with blister vacuum nozzles.
- a material transfer device for transferring the blister cards on the transiting grid conveyor device or pillow bags on the pillow bag grid conveyor device to the cartoning conveyor chain device is provided on the cartoning conveyor chain device, and the material transfer device is provided with material vacuum nozzles.
- the transiting grid conveyor device is composed of a first grid conveyor device and a second grid conveyor device, and a connecting ramp is provided between the first grid conveyor device and the second grid conveyor device.
- the high point of the connecting ramp is connected to the first grid conveyor device, and the low point of the connecting ramp is connected to the second grid conveyor device.
- the first grid conveyor device and the second grid conveyor device each are driven by an independent motor.
- the corresponding independent motors configured to provide a grid spacing of the first grid conveyor device different from a grid spacing of the second grid conveyor device, the corresponding independent motors configured to move the first grid conveyor device and the second grid conveyor device by one grid spacing in a same amount of time, and the first grid conveyor device is provided side by side with the discharging grid conveyor device.
- the grid spacing of the first grid conveyor device is the same as the grid spacing of the pillow bag conveyor chain device.
- the second grid conveyor device is provided side by side with the cartoning conveyor chain device, and the grid spacing of the second grid conveyor device is the same as the grid spacing of the cartoning conveyor chain device.
- the output end of the pillow-type packaging machine is connected to the pillow bag grid conveyor device through a rotary transfer manipulator for conveyance, and the rotary transfer manipulator may rotate pillow bags on the output end of the pillow-type packaging machine by 90° and transfer the pillow bags to the pillow bag grid conveyor device.
- the material transfer device includes a manipulator and a suction mechanism.
- the suction mechanism includes a nozzle holder and a plurality of the material vacuum nozzles.
- the material vacuum nozzles are provided on the nozzle holder.
- the nozzle holder is connected to a connecting seat, a connecting groove is formed in the connecting seat, and the connecting seat is connected to a locating pin.
- the manipulator is connected to a connecting member, a pinhole is formed in the connecting member, the connecting member is provided in the connecting groove of the connecting seat, and the locating pin may be inserted into the pinhole of the connecting member.
- a guideway is provided on the blister card transfer device.
- the blister card transfer device is slidably provided on the guideway through a sliding seat, and the blister card transfer device may move to an upward side between the discharging grid conveyor device and the transiting grid conveyor device or move to an upward side between the discharging grid conveyor device and the pillow bag conveyor chain device.
- the high-speed double-line blister and pillow bag cartoning integrated machine provided by the present disclosure can realize packaging of cartoning the blisters and packaging of cartoning the blisters and the pillow bags in a small footprint and can be switched between two different packaging forms quickly and flexibly.
- the high-speed double-line blister and pillow bag cartoning integrated machine includes blister packaging machine 1, pillow-type packaging machine 6, and cartoning machine 11.
- the blister packaging machine 1 is configured to form, package, and cut pharmaceutical blister cards.
- the pillow-type packaging machine 6 is configured to package the blister cards into packaging films to form pillow bags.
- the cartoning machine 11 is configured to package the pharmaceutical blister cards or pillow bags into cartons.
- the present disclosure provides the following technical solutions.
- the blister packaging machine 1 is connected to discharging grid conveyor device 2 for conveyance (i.e., the blister packaging machine 1 conveys the blister cards to the discharging grid conveyor device 2).
- Pillow bag conveyor chain device 3 is provided side by side at one side of the discharging grid conveyor device 2 (e.g., the pillow bag conveyor chain device 3 is also a grid conveyor device but is only provided with one row of grids).
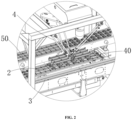
- Blister card transfer device 4 (as shown in FIG. 2 , the blister card transfer device 4 is provided with blister vacuum nozzles 40 capable of sucking the blister cards, which is the prior art) is provided on the discharging grid conveyor device 2.
- the blister card transfer device 4 can transfer the blister cards on the discharging grid conveyor device 2 to the pillow bag conveyor chain device 3.
- the pillow bag conveyor chain device 3 is connected to the pillow-type packaging machine 6 for conveyance.
- the pillow bag conveyor chain device 3 conveys the blister cards to the pillow-type packaging machine 6.
- the pillow-type packaging machine 6 packages the blister cards into the packaging films to form the pillow bags.
- An output end of the pillow-type packaging machine 6 is connected to pillow bag grid conveyor device 8 for conveyance.
- the pillow bags from the output end of the pillow-type packaging machine 6 enter the pillow bag grid conveyor device 8 and are continuously conveyed by the pillow bag grid conveyor device 8.
- cartoning conveyor chain device 10 e.g., the cartoning conveyor chain device 10 is also a grid conveyor device but is only provided with one row of grids.
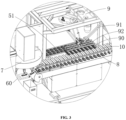
- Material transfer device 9 (as shown in FIG. 3 , the material transfer device 9 is provided with material vacuum nozzles 90 capable of sucking the blister cards or the pillow bags, which is the prior art) is provided on the cartoning conveyor chain device 10.
- the material transfer device 9 can transfer the pillow bags on the pillow bag grid conveyor device 8 to the cartoning conveyor chain device 10 (which can realize tracking and multi-bag stacking).
- the cartoning conveyor chain device 10 is connected to the cartoning machine 11 for conveyance.
- the cartoning conveyor chain device 10 conveys the pillow bags to the cartoning machine 11.
- the cartoning machine 11 packages the pillow bags into the cartons.
- the other side of the discharging grid conveyor device 2 is provided with transiting grid conveyor device 5.
- the blister card transfer device 4 can transfer the blister cards on the discharging grid conveyor device 2 to the transiting grid conveyor device 5.
- the transiting grid conveyor device 5 extends to one side of the cartoning conveyor chain device 10.
- the cartoning conveyor chain device 10 is located between the transiting grid conveyor device 5 and the pillow bag grid conveyor device 8.
- the material transfer device 9 can transfer the blister cards on the transiting grid conveyor device 5 to the cartoning conveyor chain device 10 (which can realize tracking and multi-card stacking).
- the cartoning conveyor chain device 10 conveys the blister cards to the cartoning machine 11.
- the cartoning machine 11 packages the blister cards into the cartons.
- the high-speed double-line blister and pillow bag cartoning integrated machine has a small footprint and can be switched between the packaging of cartoning the blisters and the packaging of cartoning the blisters and the pillow bags as required by the user, thereby being very convenient and flexible.
- the grid spacing of the pillow bag conveyor chain device 3 is different from the grid spacing of the cartoning conveyor chain device 10. Since the transiting grid conveyor device 5 needs to transfer the blister cards to the cartoning conveyor chain device 10, the grid spacing of the transiting grid conveyor device 5 is the same as the grid spacing of the cartoning conveyor chain device 10. In other words, normally, the grid spacing of the pillow bag conveyor chain device 3 is different from the grid spacing of the transiting grid conveyor device 5.
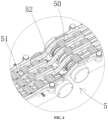
- the transiting grid conveyor device 5 is composed of first grid conveyor device 50 and second grid conveyor device 51 (both have different grid spacings).
- Connecting ramp 52 is provided between the first grid conveyor device 50 and the second grid conveyor device 51.
- the high point of the connecting ramp 52 is connected to the first grid conveyor device 50.
- the low point of the connecting ramp 52 is connected to the second grid conveyor device 51.
- the first grid conveyor device 50 and the second grid conveyor device 51 each are driven by an independent motor.
- the first grid conveyor device 50 and the second grid conveyor device 51 each work under the control of the corresponding independent motor.
- the time it takes for the first grid conveyor device 50 to move by one grid spacing is the same as the time it takes for the second grid conveyor device 51 to move by one grid spacing.
- the blister card in one grid of the first grid conveyor device 50 falls into one grid of the second grid conveyor device 51 through the connecting ramp 52.
- the first grid conveyor device 50 is provided side by side with the discharging grid conveyor device 2.
- the grid spacing of the first grid conveyor device 50 is the same as the grid spacing of the pillow bag conveyor chain device 3.
- the second grid conveyor device 51 is provided side by side with the cartoning conveyor chain device 10.
- the grid spacing of the second grid conveyor device 51 is the same as the grid spacing of the cartoning conveyor chain device 10.
- the blister cards in the two modes can be transferred through only one type of the blister card transfer device 4, and there is no need to change the suction mechanism of the blister card transfer device 4.
- the transiting grid conveyor device 5 is divided into two segments, such that the transmission chain on each segment is shorter (the grid plate is provided on the transmission chain), the transmission chain operates more stably, and the transportation on the machine is more convenient (the loading requirement cannot be met if the transiting grid conveyor device 5 is very long).
- the second grid conveyor device 51 may be divided into two segments. In this case, the transiting grid conveyor device 5 is divided into one segment of the first grid conveyor device 50 and two segments of the second grid conveyor device 51 to meet the loading requirement. It is noted that any case where the transiting grid conveyor device 5 is segmented falls within the protection scope of the present disclosure.
- the output end of the pillow-type packaging machine 6 is provided with conveyor belt 60.
- the pillow-type packaging machine 6 conveys the pillow bags through the conveyor belt 60.
- the pillow bags on the conveyor belt 60 can directly fall into the grids of the pillow bag grid conveyor device 8.
- the pillow bags from the pillow-type packaging machine 6 are horizontally arranged. According to longitudinal feeding of the cartoning machine 11, it is better to rotate the pillow bags on the conveyor belt 60 by 90° and then fall the pillow bags into the pillow bag grid conveyor device 8.
- the material transfer device 9 can directly transfer the materials on the pillow bag grid conveyor device 8 to the cartoning conveyor chain device 10.
- the output end of the pillow-type packaging machine 6 is connected to the pillow bag grid conveyor device 8 through rotary transfer manipulator 7 for conveyance.
- the rotary transfer manipulator 7 can rotate the pillow bags on the conveyor belt 60 of the pillow-type packaging machine 6 by 90° and transfer the pillow bags to the pillow bag grid conveyor device 8.
- the rotary transfer manipulator 7 is the prior art, and its structure is not described repeatedly herein. Certainly, the rotary transfer manipulator 7 may also not be used, but the material transfer device 9 sucks the pillow bags for rotation. In this case, the material transfer device 9 will be more complicated. Regardless of the manners used, all should fall within the protection scope of the present disclosure.
- the material transfer device 9 includes manipulator 91 and a suction mechanism.
- the suction mechanism includes nozzle holder 92 and a plurality of the material vacuum nozzles 90.
- the material vacuum nozzles 90 are provided on the nozzle holder 92.
- the material transfer device 9 not only transfers the pillow bags from the pillow bag grid conveyor device 8 to the cartoning conveyor chain device 10 but also transfers the blister cards from the transiting grid conveyor device 5 to the cartoning conveyor chain device 10.
- the pillow bags are conveyed in one row, while the blister cards are conveyed in multiple rows.
- the suction mechanism of the material transfer device 9 is changed.
- the nozzle holder 92 is connected to a connecting seat.
- a connecting groove is formed in the connecting seat.
- the connecting seat is connected to a locating pin.
- the manipulator 91 is connected to a connecting member.
- a pinhole is formed in the connecting member.
- the connecting member is provided in the connecting groove of the connecting seat.
- the locating pin may be inserted into the pinhole of the connecting member.
- the blister card transfer device 4 can realize tracking and multi-card stacking when transferring the blister cards. Since the pillow bag conveyor chain device 3 and the transiting grid conveyor device 5 to be tracked are respectively located on two sides of the discharging grid conveyor device 2, there is a need to locate the blister card transfer device 4 at an appropriate position. When the pillow bag conveyor chain device 3 is to be tracked, the blister card transfer device 4 is located on an upward side between the discharging grid conveyor device 2 and the pillow bag conveyor chain device 3. When the transiting grid conveyor device 5 is to be tracked, the blister card transfer device 4 is located on an upward side between the discharging grid conveyor device 2 and the transiting grid conveyor device 5. A guideway 41 is provided on the blister card transfer device 4.
- the blister card transfer device 4 is slidably provided on the guideway 41 through a sliding seat. By sliding the sliding seat, the blister card transfer device 4 may move to the upward side between the discharging grid conveyor device 2 and the transiting grid conveyor device 5 or move to the upward side between the discharging grid conveyor device 2 and the pillow bag conveyor chain device 3, thereby transferring, tracking and stacking the blister cards in different packaging manners.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Container Filling Or Packaging Operations (AREA)
- Auxiliary Devices For And Details Of Packaging Control (AREA)
Description
- The present disclosure relates to the field of pharmaceutical card packaging machines, particularly to a machine for packaging blister cards.
- In modern pharmaceutical packaging, a more flexible packaging solution for pharmaceutical blister cards is desired by pharmaceutical companies. Given the thermal sensitivity of some medicines, pharmaceutical blister cards (referred to as blisters or blister cards) not only are cartoned (e.g., the pharmaceutical blister cards are directly packaged into cartons), but also are packaged into pillow bags to be placed into cartons. In the prior art, different packaging devices are used to provide perform different packaging manners, or the pharmaceutical cards are preliminarily distributed to a rear packaging device by a conveyor belt. This increases the equipment purchasing cost of the pharmaceutical companies and requires larger equipment space, higher mounting costs, and higher equipment operation and maintenance costs. Therefore, the prior art can hardly meet the demand of modern pharmaceutical packaging for flexibility in the new era.
- The Chinese Patent Application Publication
CN 206 871 414 U discloses a high-speed double-line blister and pillow bag cartoning integrated machine, comprising a blister packaging machine, a pillow-type packaging machine, and a cartoning machine, wherein the blister packaging machine is connected to a discharging grid conveyor device for conveyance. A blister card transfer device is also included for transferring blister cards on the discharging grid conveyor device to a pillow bag conveyor chain device or a transiting grid conveyor device. - Given shortages in the prior art, the present disclosure provides a high-speed double-line blister and pillow bag cartoning integrated machine, which not only can directly carton the blisters but can also package the blisters into the pillow bags for cartoning.
- A high-speed double-line blister and pillow bag cartoning integrated machine includes a blister packaging machine, a pillow-type packaging machine, and a cartoning machine. The blister packaging machine is connected to a discharging grid conveyor device for conveyance. A pillow bag conveyor chain device is provided side by side at one side of the discharging grid conveyor device. The pillow bag conveyor chain device is connected to the pillow-type packaging machine for conveyance. An output end of the pillow-type packaging machine is connected to a pillow bag grid conveyor device for conveyance. One side of the pillow bag grid conveyor device is provided with a cartoning conveyor chain device, and the cartoning conveyor chain device is connected to the cartoning machine for conveyance. The other side of the discharging grid conveyor device is provided with a transiting grid conveyor device. The transiting grid conveyor device extends to one side of the cartoning conveyor chain device, and the cartoning conveyor chain device is located between the transiting grid conveyor device and the pillow bag grid conveyor device. A blister card transfer device for transferring blister cards on the discharging grid conveyor device to the pillow bag conveyor chain device or the transiting grid conveyor device is provided on the discharging grid conveyor device, and the blister card transfer device is provided with blister vacuum nozzles. A material transfer device for transferring the blister cards on the transiting grid conveyor device or pillow bags on the pillow bag grid conveyor device to the cartoning conveyor chain device is provided on the cartoning conveyor chain device, and the material transfer device is provided with material vacuum nozzles. The transiting grid conveyor device is composed of a first grid conveyor device and a second grid conveyor device, and a connecting ramp is provided between the first grid conveyor device and the second grid conveyor device. The high point of the connecting ramp is connected to the first grid conveyor device, and the low point of the connecting ramp is connected to the second grid conveyor device. The first grid conveyor device and the second grid conveyor device each are driven by an independent motor. The corresponding independent motors configured to provide a grid spacing of the first grid conveyor device different from a grid spacing of the second grid conveyor device, the corresponding independent motors configured to move the first grid conveyor device and the second grid conveyor device by one grid spacing in a same amount of time, and the first grid conveyor device is provided side by side with the discharging grid conveyor device. The grid spacing of the first grid conveyor device is the same as the grid spacing of the pillow bag conveyor chain device. The second grid conveyor device is provided side by side with the cartoning conveyor chain device, and the grid spacing of the second grid conveyor device is the same as the grid spacing of the cartoning conveyor chain device.
- The output end of the pillow-type packaging machine is connected to the pillow bag grid conveyor device through a rotary transfer manipulator for conveyance, and the rotary transfer manipulator may rotate pillow bags on the output end of the pillow-type packaging machine by 90° and transfer the pillow bags to the pillow bag grid conveyor device.
- The material transfer device includes a manipulator and a suction mechanism. The suction mechanism includes a nozzle holder and a plurality of the material vacuum nozzles. The material vacuum nozzles are provided on the nozzle holder. The nozzle holder is connected to a connecting seat, a connecting groove is formed in the connecting seat, and the connecting seat is connected to a locating pin. The manipulator is connected to a connecting member, a pinhole is formed in the connecting member, the connecting member is provided in the connecting groove of the connecting seat, and the locating pin may be inserted into the pinhole of the connecting member.
- A guideway is provided on the blister card transfer device. The blister card transfer device is slidably provided on the guideway through a sliding seat, and the blister card transfer device may move to an upward side between the discharging grid conveyor device and the transiting grid conveyor device or move to an upward side between the discharging grid conveyor device and the pillow bag conveyor chain device.
- The high-speed double-line blister and pillow bag cartoning integrated machine provided by the present disclosure can realize packaging of cartoning the blisters and packaging of cartoning the blisters and the pillow bags in a small footprint and can be switched between two different packaging forms quickly and flexibly.
-
-
FIG. 1 is a top view of the present disclosure; -
FIG. 2 is an operation view of a blister card transfer device; -
FIG. 3 is an operation view of a material transfer device; and -
FIG. 4 is a side view of a transiting grid conveyor device. - As shown in
FIG. 1 , the high-speed double-line blister and pillow bag cartoning integrated machine includes blister packaging machine 1, pillow-type packaging machine 6, and cartoning machine 11. The blister packaging machine 1 is configured to form, package, and cut pharmaceutical blister cards. The pillow-type packaging machine 6 is configured to package the blister cards into packaging films to form pillow bags. The cartoning machine 11 is configured to package the pharmaceutical blister cards or pillow bags into cartons. - To link the blister packaging machine 1, the pillow-type packaging machine 6, and the cartoning machine 11 and realize a packaging manner of cartoning the blisters and a packaging manner of cartoning the blisters and the pillow bags, the present disclosure provides the following technical solutions.
- For the packaging manner of cartoning the blisters and the pillow bags: As shown in
FIG. 1 , the blister packaging machine 1 is connected to discharginggrid conveyor device 2 for conveyance (i.e., the blister packaging machine 1 conveys the blister cards to the discharging grid conveyor device 2). Pillow bagconveyor chain device 3 is provided side by side at one side of the discharging grid conveyor device 2 (e.g., the pillow bagconveyor chain device 3 is also a grid conveyor device but is only provided with one row of grids). Blister card transfer device 4 (as shown inFIG. 2 , the blistercard transfer device 4 is provided withblister vacuum nozzles 40 capable of sucking the blister cards, which is the prior art) is provided on the discharginggrid conveyor device 2. The blistercard transfer device 4 can transfer the blister cards on the discharginggrid conveyor device 2 to the pillow bagconveyor chain device 3. The pillow bagconveyor chain device 3 is connected to the pillow-type packaging machine 6 for conveyance. The pillow bagconveyor chain device 3 conveys the blister cards to the pillow-type packaging machine 6. The pillow-type packaging machine 6 packages the blister cards into the packaging films to form the pillow bags. An output end of the pillow-type packaging machine 6 is connected to pillow baggrid conveyor device 8 for conveyance. The pillow bags from the output end of the pillow-type packaging machine 6 enter the pillow baggrid conveyor device 8 and are continuously conveyed by the pillow baggrid conveyor device 8. One side of the pillow baggrid conveyor device 8 is provided with cartoning conveyor chain device 10 (e.g., the cartoningconveyor chain device 10 is also a grid conveyor device but is only provided with one row of grids). Material transfer device 9 (as shown inFIG. 3 , thematerial transfer device 9 is provided withmaterial vacuum nozzles 90 capable of sucking the blister cards or the pillow bags, which is the prior art) is provided on the cartoningconveyor chain device 10. Thematerial transfer device 9 can transfer the pillow bags on the pillow baggrid conveyor device 8 to the cartoning conveyor chain device 10 (which can realize tracking and multi-bag stacking). The cartoningconveyor chain device 10 is connected to the cartoning machine 11 for conveyance. The cartoningconveyor chain device 10 conveys the pillow bags to the cartoning machine 11. The cartoning machine 11 packages the pillow bags into the cartons. With the above structure, the packaging manner of cartoning the blisters and the pillow bags can be realized. - For the packaging manner of cartoning the blisters: As shown in
FIG. 1 , the other side of the discharginggrid conveyor device 2 is provided with transitinggrid conveyor device 5. The blistercard transfer device 4 can transfer the blister cards on the discharginggrid conveyor device 2 to the transitinggrid conveyor device 5. The transitinggrid conveyor device 5 extends to one side of the cartoningconveyor chain device 10. The cartoningconveyor chain device 10 is located between the transitinggrid conveyor device 5 and the pillow baggrid conveyor device 8. Thematerial transfer device 9 can transfer the blister cards on the transitinggrid conveyor device 5 to the cartoning conveyor chain device 10 (which can realize tracking and multi-card stacking). The cartoningconveyor chain device 10 conveys the blister cards to the cartoning machine 11. The cartoning machine 11 packages the blister cards into the cartons. With the above structure, the packaging manner of cartoning the blisters can be realized. - The high-speed double-line blister and pillow bag cartoning integrated machine has a small footprint and can be switched between the packaging of cartoning the blisters and the packaging of cartoning the blisters and the pillow bags as required by the user, thereby being very convenient and flexible.
- As shown in
FIG. 1 , since there are different requirements for the spacing between materials in the pillow-type packaging machine 6 and the spacing between materials in the cartoning machine 11, the grid spacing of the pillow bagconveyor chain device 3 is different from the grid spacing of the cartoningconveyor chain device 10. Since the transitinggrid conveyor device 5 needs to transfer the blister cards to the cartoningconveyor chain device 10, the grid spacing of the transitinggrid conveyor device 5 is the same as the grid spacing of the cartoningconveyor chain device 10. In other words, normally, the grid spacing of the pillow bagconveyor chain device 3 is different from the grid spacing of the transitinggrid conveyor device 5. When different packaging manners are switched, it is essential to change the suction mechanism of the blistercard transfer device 4, such that matched spacing is provided between the blister vacuum nozzles on the suction mechanism, which is inconvenient. - To solve the problem above, as shown in
FIG. 4 , the transitinggrid conveyor device 5 is composed of firstgrid conveyor device 50 and second grid conveyor device 51 (both have different grid spacings). Connectingramp 52 is provided between the firstgrid conveyor device 50 and the secondgrid conveyor device 51. The high point of the connectingramp 52 is connected to the firstgrid conveyor device 50. The low point of the connectingramp 52 is connected to the secondgrid conveyor device 51. In addition, the firstgrid conveyor device 50 and the secondgrid conveyor device 51 each are driven by an independent motor. The firstgrid conveyor device 50 and the secondgrid conveyor device 51 each work under the control of the corresponding independent motor. The time it takes for the firstgrid conveyor device 50 to move by one grid spacing is the same as the time it takes for the secondgrid conveyor device 51 to move by one grid spacing. In this case, the blister card in one grid of the firstgrid conveyor device 50 falls into one grid of the secondgrid conveyor device 51 through the connectingramp 52. Certainly, the firstgrid conveyor device 50 is provided side by side with the discharginggrid conveyor device 2. The grid spacing of the firstgrid conveyor device 50 is the same as the grid spacing of the pillow bagconveyor chain device 3. The secondgrid conveyor device 51 is provided side by side with the cartoningconveyor chain device 10. The grid spacing of the secondgrid conveyor device 51 is the same as the grid spacing of the cartoningconveyor chain device 10. - With the above structure, the blister cards in the two modes can be transferred through only one type of the blister
card transfer device 4, and there is no need to change the suction mechanism of the blistercard transfer device 4. The transitinggrid conveyor device 5 is divided into two segments, such that the transmission chain on each segment is shorter (the grid plate is provided on the transmission chain), the transmission chain operates more stably, and the transportation on the machine is more convenient (the loading requirement cannot be met if the transitinggrid conveyor device 5 is very long). Certainly, if the transitinggrid conveyor device 5 is still too long after being divided into two segments, the secondgrid conveyor device 51 may be divided into two segments. In this case, the transitinggrid conveyor device 5 is divided into one segment of the firstgrid conveyor device 50 and two segments of the secondgrid conveyor device 51 to meet the loading requirement. It is noted that any case where the transitinggrid conveyor device 5 is segmented falls within the protection scope of the present disclosure. - As shown in
FIG. 3 , the output end of the pillow-type packaging machine 6 is provided withconveyor belt 60. The pillow-type packaging machine 6 conveys the pillow bags through theconveyor belt 60. The pillow bags on theconveyor belt 60 can directly fall into the grids of the pillow baggrid conveyor device 8. However, the pillow bags from the pillow-type packaging machine 6 are horizontally arranged. According to longitudinal feeding of the cartoning machine 11, it is better to rotate the pillow bags on theconveyor belt 60 by 90° and then fall the pillow bags into the pillow baggrid conveyor device 8. In this case, thematerial transfer device 9 can directly transfer the materials on the pillow baggrid conveyor device 8 to the cartoningconveyor chain device 10. The output end of the pillow-type packaging machine 6 is connected to the pillow baggrid conveyor device 8 throughrotary transfer manipulator 7 for conveyance. Therotary transfer manipulator 7 can rotate the pillow bags on theconveyor belt 60 of the pillow-type packaging machine 6 by 90° and transfer the pillow bags to the pillow baggrid conveyor device 8. Therotary transfer manipulator 7 is the prior art, and its structure is not described repeatedly herein. Certainly, therotary transfer manipulator 7 may also not be used, but thematerial transfer device 9 sucks the pillow bags for rotation. In this case, thematerial transfer device 9 will be more complicated. Regardless of the manners used, all should fall within the protection scope of the present disclosure. - As shown in
FIG. 3 , thematerial transfer device 9 includesmanipulator 91 and a suction mechanism. The suction mechanism includesnozzle holder 92 and a plurality of thematerial vacuum nozzles 90. Thematerial vacuum nozzles 90 are provided on thenozzle holder 92. As mentioned above, thematerial transfer device 9 not only transfers the pillow bags from the pillow baggrid conveyor device 8 to the cartoningconveyor chain device 10 but also transfers the blister cards from the transitinggrid conveyor device 5 to the cartoningconveyor chain device 10. The pillow bags are conveyed in one row, while the blister cards are conveyed in multiple rows. Hence, when the packaging manner is switched, the suction mechanism of thematerial transfer device 9 is changed. To quickly change the suction mechanism, thenozzle holder 92 is connected to a connecting seat. A connecting groove is formed in the connecting seat. The connecting seat is connected to a locating pin. Themanipulator 91 is connected to a connecting member. A pinhole is formed in the connecting member. The connecting member is provided in the connecting groove of the connecting seat. The locating pin may be inserted into the pinhole of the connecting member. When the suction mechanism is changed, the connecting member on themanipulator 91 is clamped into the connecting groove of the connecting seat, and the locating pin is inserted into the pinhole of the connecting member, which is very convenient and quick. - Finally, it is worth noting that the blister
card transfer device 4 can realize tracking and multi-card stacking when transferring the blister cards. Since the pillow bagconveyor chain device 3 and the transitinggrid conveyor device 5 to be tracked are respectively located on two sides of the discharginggrid conveyor device 2, there is a need to locate the blistercard transfer device 4 at an appropriate position. When the pillow bagconveyor chain device 3 is to be tracked, the blistercard transfer device 4 is located on an upward side between the discharginggrid conveyor device 2 and the pillow bagconveyor chain device 3. When the transitinggrid conveyor device 5 is to be tracked, the blistercard transfer device 4 is located on an upward side between the discharginggrid conveyor device 2 and the transitinggrid conveyor device 5. Aguideway 41 is provided on the blistercard transfer device 4. The blistercard transfer device 4 is slidably provided on theguideway 41 through a sliding seat. By sliding the sliding seat, the blistercard transfer device 4 may move to the upward side between the discharginggrid conveyor device 2 and the transitinggrid conveyor device 5 or move to the upward side between the discharginggrid conveyor device 2 and the pillow bagconveyor chain device 3, thereby transferring, tracking and stacking the blister cards in different packaging manners.
Claims (4)
- A high-speed double-line integrated blister and pillow bag cartoning machine, comprising a blister packaging machine (1), a pillow-type packaging machine (6), and a cartoning machine (11), wherein the blister packaging machine (1) is connected to a discharging grid conveyor device (2) and a pillow bag conveyor chain device (3) is arranged at one side of the discharging grid conveyor device (2), the pillow bag conveyor chain device (3) is connected to the pillow-type packaging machine (6) wherein an output end of the pillow-type packaging machine (6) is connected to a pillow bag grid conveyor device (8), at one side of the pillow bag grid conveyor device (8) a cartoning conveyor chain device (10) is arranged, and the cartoning conveyor chain device (10) is connected to the cartoning machine (11) wherein at the other side of the discharging grid conveyor device (2) a transiting grid conveyor device (5) is arranged and the transiting grid conveyor device (5) extends to one side of the cartoning conveyor chain device (10), and the cartoning conveyor chain device (10) is located between the transiting grid conveyor device (5) and the pillow bag grid conveyor device (8) wherein a blister card transfer device (4) adapted to transfer blister cards on the discharging grid conveyor device (2) to the pillow bag conveyor chain device (3) or to the transiting grid conveyor device (5) is arranged over the discharging grid conveyor device (2), characterized in that the blister card transfer device (4) is provided with blister vacuum nozzles (40); and a material transfer device (9) is adapted to transfer the blister cards on the transiting grid conveyor device (5) or pillow bags on the pillow bag grid conveyor device (8) to the cartoning conveyor chain device (10) is arranged over the cartoning conveyor chain device (10), and the material transfer device (9) is provided with material vacuum nozzles (90), wherein the transiting grid conveyor device (5) is composed of a first grid conveyor device (50) and a second grid conveyor device (51), wherein a connecting ramp (52) is provided between the first grid conveyor device (50) and the second grid conveyor device (51), a high point of the connecting ramp (52) is connected to the first grid conveyor device (50), a low point of the connecting ramp (52) is connected to the second grid conveyor device (51), the first grid conveyor device (50) and the second grid conveyor device (51) each are driven by an independent motor wherein the grid spacing of the first grid conveyor device (50) is different from the grid spacing of the second grid conveyor device (51) wherein the corresponding independent motors are configured to move the first grid conveyor device (50) and the second grid conveyor device (51) by one grid spacing in the same amount of time, wherein the first grid conveyor device (50) is provided side by side with the discharging grid conveyor device (2), the grid spacing of the first grid conveyor device (50) is same as the grid spacing of the pillow bag conveyor chain device (3), the second grid conveyor device (51) is provided side by side with the cartoning conveyor chain device (10), and the grid spacing of the second grid conveyor device (51) is same as the grid spacing of the cartoning conveyor chain device (10).
- The high-speed double-line integrated blister and pillow bag cartoning machine according to claim 1, wherein the output end of the pillow-type packaging machine (6) is connected to the pillow bag grid conveyor device (8) through a rotary transfer manipulator (7) Bayramoglu Patent ve Marka Danismanlik Limited Sirketi, Mira Office, Kanuni Sultan Su!eyman Boulevard, 5387. Street, Beytepe, floor 12, no:50 Cankaya/Ankara, Turkey and the rotary transfer manipulator (7) is adapted to rotate the pillow bags on the output end of the pillow-type packaging machine (6) by 90° and to transfer the pillow bags to the pillow bag grid conveyor device (8).
- The high-speed double-line integrated blister and pillow bag cartoning machine according to claim 1, wherein the material transfer device (9) comprises a manipulator (91) and a suction mechanism, the suction mechanism comprises a nozzle holder (92) and a plurality of material vacuum nozzles (90), the material vacuum nozzles (90) are provided on the nozzle holder (92), the nozzle holder (92) is connected to a connecting seat, wherein a connecting groove is formed in the connecting seat, the connecting seat is connected to a locating pin, the manipulator (91) is connected to a connecting member, a pinhole is formed in the connecting member, the connecting member is provided in the connecting groove of the connecting seat, and the locating pin is inserted into the pinhole of the connecting member.
- The high-speed double-line integrated blister and pillow bag cartoning machine according to claim 1, wherein a guideway (41) is provided on the blister card transfer device (4), the blister card transfer device (4) is slidably provided on the guideway (41) through a sliding seat, and the blister card transfer device (4) is adapted to move between the discharging grid conveyor device (2) and the transiting grid conveyor device (5) or to move between the discharging grid conveyor device (2) and the pillow bag conveyor chain device (3) on the upper side.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202111669179.6A CN114313363A (en) | 2021-12-31 | 2021-12-31 | High-speed double-line bubble cap pillow packaging box all-in-one machine |
| PCT/CN2022/109316 WO2023124067A1 (en) | 2021-12-31 | 2022-07-31 | High-speed double-track blister pillow packing and cartoning packing integrated machine |
Publications (4)
| Publication Number | Publication Date |
|---|---|
| EP4227229A1 EP4227229A1 (en) | 2023-08-16 |
| EP4227229A4 EP4227229A4 (en) | 2024-04-10 |
| EP4227229B1 true EP4227229B1 (en) | 2024-10-09 |
| EP4227229B8 EP4227229B8 (en) | 2024-11-13 |
Family
ID=81020963
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP22850634.1A Active EP4227229B8 (en) | 2021-12-31 | 2022-07-31 | High-speed double-line blister and pillow bag cartoning integrated machine |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP4227229B8 (en) |
| CN (1) | CN114313363A (en) |
| WO (1) | WO2023124067A1 (en) |
Families Citing this family (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114313363A (en) * | 2021-12-31 | 2022-04-12 | 浙江希望机械有限公司 | High-speed double-line bubble cap pillow packaging box all-in-one machine |
| CN118124887A (en) * | 2024-04-12 | 2024-06-04 | 浙江瑞安华联药机科技有限公司 | A medicine board box packaging production line |
Family Cites Families (20)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE10026497A1 (en) * | 2000-05-27 | 2001-11-29 | Bosch Gmbh Robert | Blister strip feed device for packing machine has additional post-fitting laying and separating elements |
| CN100410147C (en) * | 2005-06-03 | 2008-08-13 | 浙江圣雷机械有限公司 | Automatic dispensing and conveying mechanism for medicine plate loading |
| GB0916966D0 (en) * | 2009-09-28 | 2009-11-11 | Meadwestvaco Packaging Systems | Packaging machine |
| GB201118710D0 (en) * | 2011-10-28 | 2011-12-14 | Meadwestvaco Packaging Systems | Packaging system,machine and transfer apparatus |
| EP2840029A1 (en) * | 2013-08-23 | 2015-02-25 | UHLMANN PAC-SYSTEME GmbH & Co. KG | Device for transferring blister packs |
| CN205023009U (en) * | 2015-08-17 | 2016-02-10 | 杭州永创智能设备股份有限公司 | Bubble cap dress box all -in -one |
| EP3266718B1 (en) * | 2016-07-08 | 2018-07-25 | Mediseal GmbH | Packaging machine including a temporary storage unit for packed medical goods |
| EP3339192B1 (en) * | 2016-12-21 | 2019-03-06 | UHLMANN PAC-SYSTEME GmbH & Co. KG | Method for transferring blister packs |
| CN106956796B (en) * | 2017-05-03 | 2022-12-30 | 浙江希望机械有限公司 | High-speed bubble cap pillow packing box all-in-one |
| CN206871414U (en) * | 2017-05-03 | 2018-01-12 | 浙江希望机械有限公司 | High speed bubble-cap rests the head on packing box all-in-one |
| EP3560846B1 (en) * | 2018-04-23 | 2024-08-07 | Uhlmann Pac-Systeme GmbH & Co. KG | Method and device for transferring blister packs |
| CN109436436B (en) * | 2018-11-20 | 2023-08-18 | 浙江希望机械有限公司 | Partition type grid conveying system |
| CN109436437B (en) * | 2018-12-22 | 2023-08-22 | 浙江希望机械有限公司 | High-speed bubble cap boxing all-in-one machine |
| CN210555994U (en) * | 2019-06-06 | 2020-05-19 | 上海爱的发制药有限公司 | Medicine board detects quick-witted on-line pillow packagine machine box packing machine layout structure |
| DE102019006687A1 (en) * | 2019-09-24 | 2021-03-25 | Focke & Co. (Gmbh & Co. Kg) | Method for inserting inner packs into an outer pack |
| CN211687311U (en) * | 2019-11-28 | 2020-10-16 | 东莞市键环自动化设备科技有限公司 | Transformer conveying mechanism |
| CN112938004A (en) * | 2021-04-25 | 2021-06-11 | 浙江希望机械有限公司 | Bubble cap plate transfer device |
| CN112918760B (en) * | 2021-04-25 | 2026-01-13 | 浙江希望机械有限公司 | Bubble cap pillow packaging box all-in-one machine |
| CN113023003B (en) * | 2021-05-12 | 2025-02-14 | 浙江海晨机械有限公司 | A fully automatic pre-filled needle packaging production line |
| CN114313363A (en) * | 2021-12-31 | 2022-04-12 | 浙江希望机械有限公司 | High-speed double-line bubble cap pillow packaging box all-in-one machine |
-
2021
- 2021-12-31 CN CN202111669179.6A patent/CN114313363A/en active Pending
-
2022
- 2022-07-31 WO PCT/CN2022/109316 patent/WO2023124067A1/en not_active Ceased
- 2022-07-31 EP EP22850634.1A patent/EP4227229B8/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| WO2023124067A1 (en) | 2023-07-06 |
| EP4227229A4 (en) | 2024-04-10 |
| CN114313363A (en) | 2022-04-12 |
| EP4227229B8 (en) | 2024-11-13 |
| EP4227229A1 (en) | 2023-08-16 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP4227229A1 (en) | High-speed double-track blister pillow packing and cartoning packing integrated machine | |
| CN104364161B (en) | Packaging assembly, in particular cartoning assembly | |
| CA2053720C (en) | Multi-purpose stacker with overlapping material handling devices | |
| US7584589B2 (en) | Robotic multi-product case-packing system | |
| EP0588298B1 (en) | An apparatus for grouping objects | |
| US20110083939A1 (en) | Device and Method for Composing Packages for a Packaging Machine | |
| US8393132B2 (en) | Device and method for filling containers | |
| EP2204280A2 (en) | Method and apparatus for supplying bags to a packaging machine | |
| CN107572027A (en) | The method of labelling machine and production multi-pack | |
| CN108298133B (en) | Method for transferring blister packs | |
| US20160236809A1 (en) | Object carrier and packaging system | |
| CA2176489C (en) | Envelope-stuffing device | |
| EP1164081A1 (en) | Bag transfer device for automatic packaging machines | |
| SE408882B (en) | DEVICE FOR FEEDING AND GROUPING OF FOREMAL ON A PLANT SURFACE | |
| CN212423657U (en) | Bag opening device and packaging system | |
| JP2022143193A (en) | Array apparatus and boxing system | |
| CN217706472U (en) | Robot case packer | |
| CN215884250U (en) | Feeding assembly of box packing machine and box packing machine | |
| RU2802525C1 (en) | High speed double line integrated blister and pillow bag box packing machine | |
| CN212402785U (en) | Label releasing mechanism and packaging system | |
| CN108971004A (en) | A kind of automatic sorting device of logistics package | |
| US7395915B2 (en) | Article transport, meterer and loader | |
| CN212606111U (en) | Station board and conveying mechanism for soft bag boxing machine | |
| CN209870916U (en) | Automatic boxing and stacking integrated line based on stacking robot | |
| CN101973408A (en) | Tongue depressor positioning and pushing device for tongue depressor packaging machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: UNKNOWN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20230207 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R079 Free format text: PREVIOUS MAIN CLASS: B65B0011520000 Ipc: B65B0035440000 Ref country code: DE Ref legal event code: R079 Ref document number: 602022006740 Country of ref document: DE Free format text: PREVIOUS MAIN CLASS: B65B0011520000 Ipc: B65B0035440000 |
|
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20240311 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B65B 65/00 20060101ALI20240304BHEP Ipc: B65B 35/24 20060101ALI20240304BHEP Ipc: B65B 35/18 20060101ALI20240304BHEP Ipc: B65B 35/38 20060101ALI20240304BHEP Ipc: B65B 35/44 20060101AFI20240304BHEP |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| INTG | Intention to grant announced |
Effective date: 20240711 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Free format text: CASE NUMBER: APP_49308/2024 Effective date: 20240829 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PK Free format text: BERICHTIGUNG B8 Ref country code: DE Ref legal event code: R096 Ref document number: 602022006740 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20241009 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1730371 Country of ref document: AT Kind code of ref document: T Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250209 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250210 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250110 Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250109 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602022006740 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20241009 |
|
| 26N | No opposition filed |
Effective date: 20250710 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20250627 Year of fee payment: 4 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250731 Year of fee payment: 4 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: H13 Free format text: ST27 STATUS EVENT CODE: U-0-0-H10-H13 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260224 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250731 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20250731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250731 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20250731 |