EP3663444B1 - Air spinning method for the production of large yarns with count lower than ne20 and respective yarn - Google Patents
Air spinning method for the production of large yarns with count lower than ne20 and respective yarn Download PDFInfo
- Publication number
- EP3663444B1 EP3663444B1 EP19212913.8A EP19212913A EP3663444B1 EP 3663444 B1 EP3663444 B1 EP 3663444B1 EP 19212913 A EP19212913 A EP 19212913A EP 3663444 B1 EP3663444 B1 EP 3663444B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- fibers
- yarn
- spinning
- air
- air spinning
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- D—TEXTILES; PAPER
- D02—YARNS; MECHANICAL FINISHING OF YARNS OR ROPES; WARPING OR BEAMING
- D02G—CRIMPING OR CURLING FIBRES, FILAMENTS, THREADS, OR YARNS; YARNS OR THREADS
- D02G3/00—Yarns or threads, e.g. fancy yarns; Processes or apparatus for the production thereof, not otherwise provided for
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H1/00—Spinning or twisting machines in which the product is wound-up continuously
- D01H1/11—Spinning by false-twisting
- D01H1/115—Spinning by false-twisting using pneumatic means
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H1/00—Spinning or twisting machines in which the product is wound-up continuously
- D01H1/11—Spinning by false-twisting
-
- D—TEXTILES; PAPER
- D01—NATURAL OR MAN-MADE THREADS OR FIBRES; SPINNING
- D01H—SPINNING OR TWISTING
- D01H4/00—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques
- D01H4/02—Open-end spinning machines or arrangements for imparting twist to independently moving fibres separated from slivers; Piecing arrangements therefor; Covering endless core threads with fibres by open-end spinning techniques imparting twist by a fluid, e.g. air vortex
-
- D—TEXTILES; PAPER
- D02—YARNS; MECHANICAL FINISHING OF YARNS OR ROPES; WARPING OR BEAMING
- D02G—CRIMPING OR CURLING FIBRES, FILAMENTS, THREADS, OR YARNS; YARNS OR THREADS
- D02G3/00—Yarns or threads, e.g. fancy yarns; Processes or apparatus for the production thereof, not otherwise provided for
- D02G3/22—Yarns or threads characterised by constructional features, e.g. blending, filament/fibre
- D02G3/36—Cored or coated yarns or threads
-
- D—TEXTILES; PAPER
- D02—YARNS; MECHANICAL FINISHING OF YARNS OR ROPES; WARPING OR BEAMING
- D02G—CRIMPING OR CURLING FIBRES, FILAMENTS, THREADS, OR YARNS; YARNS OR THREADS
- D02G3/00—Yarns or threads, e.g. fancy yarns; Processes or apparatus for the production thereof, not otherwise provided for
- D02G3/22—Yarns or threads characterised by constructional features, e.g. blending, filament/fibre
- D02G3/38—Threads in which fibres, filaments, or yarns are wound with other yarns or filaments, e.g. wrap yarns, i.e. strands of filaments or staple fibres are wrapped by a helically wound binder yarn
-
- D—TEXTILES; PAPER
- D02—YARNS; MECHANICAL FINISHING OF YARNS OR ROPES; WARPING OR BEAMING
- D02G—CRIMPING OR CURLING FIBRES, FILAMENTS, THREADS, OR YARNS; YARNS OR THREADS
- D02G1/00—Producing crimped or curled fibres, filaments, yarns, or threads, giving them latent characteristics
- D02G1/16—Producing crimped or curled fibres, filaments, yarns, or threads, giving them latent characteristics using jets or streams of turbulent gases, e.g. air, steam
- D02G1/168—Producing crimped or curled fibres, filaments, yarns, or threads, giving them latent characteristics using jets or streams of turbulent gases, e.g. air, steam including drawing or stretching on the same machine
Definitions
- the present invention relates to an air spinning method for the production of yarns with a count lower than or equal to Ne20 (295.25 dtex) and greater than or equal to Ne10 (590.5 dtex), and a relative yarn obtained with said method.
- WO-A-00/03078 and EP-A-3 330 416 disclose an air jet spun yarn having a count of Ne20.
- the yarns that are normally processed on air-spinning machines are PES, Viscose (and its modal, tencel variants, etc.), cotton and the various compounds.
- first formula can be used in the case of artificial fibers, the second for cotton.
- reference numeral 4 indicates a yarn obtained by means of an air spinning, preferably with multiple feeding.
- the present invention finds application in the use on man-made/synthetic fibers and possibly fibers mixed with cotton, but not 100% cotton.
- the yarn 4 comprises a plurality of threads 8 each comprising a plurality of fibers 12.
- a plurality of fibers 12 can be seen which can be divided into external fibers 16 and internal fibers 20.
- the internal fibers 20 are those which constitute the core of the thread 8 in turn surrounded by the external fibers 16.
- the present invention provides to obtain yarns 4 with an overall number of fibers 12 lower than 200.
- the optimum is to have a number of fibers 12 sufficient to give substance to the thread 8 but not too high to worsen its technical features.
- a yarn Pes 100% of count Ne20 (295.25 dtex), produced with air spinning machines, has a fiber length of 38mm and a section of 1.3 dtex and contains about 227 fibers.
- the solution of the present invention provides instead to maintain the fibers 12 under 200 units (maximum value) and the reason is shown in figures 3a, 3b .
- a yarn with a count Ne20 (295.25 dtex) is ideally represented, made with 1.5 dtex fibers ( figure 3a ) and 1 .0 dtex fibers ( figure 3b ). It is clearly seen that in the first case ( figure 3a ), having fibers of an average greater diameter, the number of external fibers 16 or twisted, which are wound, with respect to the internal ones 20 which remain neutral, is much higher than in the second case ( figure 3b ), where the individual fibers 12 (whether they are external fibers 16 or internal fibers 20) have a lower average diameter.
- the present invention ( figure 3a ), as the counts decrease, provides to increase the section of the fibers 12 used and therefore reduce the total number thereof, to below 200.
- the air spinning method provides the steps of preparing at least one web of textile fibers N1, to be fed by at least one introducer element 24 upstream of an air spinning device 28.
- the web N1 is previously drawn with at least one drawing device 32, and then, after drawing, said web N1 is fed into a spinning chamber 36 of an air spinning device 28.
- the fibers 12 are spun by means of jets of compressed air, so as to obtain a yarn 4 comprising internal fibers 20 surrounded by external fibers 16, in which the yarn has an overall count lower than or equal to Ne20 (295.25 dtex) of and greater than or equal to Ne10 (590.5 dtex), and in which the total number of internal and external fibers is less than 200.
- the working pressures i.e. the jets of compressed air inside the spinning chamber 36, are between 0.45 and 0.6 MPa, i.e. between 4.5 and 6 bar.
- the working speeds of the compressed air leaving the relative jets are comprised between 400 m/min and 500 m/min.
- the air-jet spinning method according to the invention allows the drawbacks of the prior art to be overcome.
- the present invention allows obtaining, by means of air spinning, yarns with a count lower than or equal to Ne20 (295.25 dtex) and greater than or equal to Ne10 (590.5 dtex). These yarns have features of resistance and elasticity which are superior to the solutions obtainable with the methods of the prior art.
- this aspect determines the improvement of the mechanical features of the yarn obtained.
- the section increase becomes extremely useful in synthetic fibers where the value of the elongation at break increases with the increase in the section of the fibers: therefore more resistance and more elasticity are obtained and, consequently, even greater quality and workability of the same yarn.
- the present invention goes against the known and consolidated idea in the art of increasing the number of fibers in yarns in order to improve the strength and elasticity of the yarn produced.
- the present invention teaches exactly the opposite, namely to decrease the number of fibers in the yarns, increasing their average size, in order to improve their mechanical and workability features. Such teaching finds advantageous application in the air-jet spinning sector.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Textile Engineering (AREA)
- Yarns And Mechanical Finishing Of Yarns Or Ropes (AREA)
- Spinning Or Twisting Of Yarns (AREA)
- Physics & Mathematics (AREA)
- Fluid Mechanics (AREA)
Description
- The present invention relates to an air spinning method for the production of yarns with a count lower than or equal to Ne20 (295.25 dtex) and greater than or equal to Ne10 (590.5 dtex), and a relative yarn obtained with said method.
- In particular, the air spinning of yarns having lower counts than Ne20 is complicated since the tenacity and regularity of the yarn tend to decrease drastically when making yarns with such low counts.
-
WO-A-00/03078 EP-A-3 330 416 disclose an air jet spun yarn having a count of Ne20. - Nazan Erdumlu et al. "The structure and properties of carded cotton vortex yarns" in the Textile Research Journal, vol. 82, no 7 describes a 100% cotton vortex yarn with a Ne20 count.
- The yarns that are normally processed on air-spinning machines are PES, Viscose (and its modal, tencel variants, etc.), cotton and the various compounds.
- The prior art of the production of such yarns involves the use of high quality fiber webs, that is with an average length of 38mm and fiber diameter between 1.3 and 1.5 dtex for artificial fibers and, in the case of cotton, with micronair lower than 4.2.
- An empirical formula defines the following link: micronair = 2,824deniers = 2,824*1,111dtex; so it follows that: dtex = micronair/3,135.
- The commonly accepted idea in the art is that in air spinning machines it is necessary to have many fibers, indeed, as many fibers as possible to obtain yarn with high strength and elasticity.
- The formula that calculates the number of fibers per section is given as follows:
Number_fibers_section=5917/(Yarn_Count (Ne) *fibre_count (dt ex))=15030/(Yarn_Count(Ne)*micronair(µ)). - Clearly the first formula can be used in the case of artificial fibers, the second for cotton.
- There are even formulas of the American Ministry of Agriculture which provide the maximum tenacity that can be reached in spinning as a function, among the various parameters, of the number of fibers that contribute to the formation of the yarn.
- This formula of the American FDA, valid for ring cotton carded yarns is the following:
Expected_Yarn_Resistance (cN/tex) =(1/count(Ne))*(19- 52*Count(Ne)+6618*Fiber_length(Inches)- 236*micronair(µ)+51*Fiber_resistance(g/tex). - From the above formula, considering that lower micronair values mean longer and more resistant fibers, it is evident that greater resistances are obtained with lower micronairs.
- Therefore, summarizing, the idea of increasing the number of fibers in yarns in order to improve the strength and elasticity of the yarn produced is known and consolidated in the art.
- Thus the idea of making yarns with a low count, with a high number of fibers, in which said fibers are relatively thin, to increase their mechanical strength, is consolidated in the art.
- It has instead been verified that this solution, in the case of applications with air spinning, does not always give the optimum compromise between strength and quality of the yarn thus obtained.
- The need to solve the drawbacks and limitations mentioned with reference to the prior art is therefore felt. Such a need is met by an air spinning method according to claim 1 and by a yarn obtained by the air spinning method according to claim 6.
- Further features and advantages of the present invention will appear more clearly from the following description of preferred non-limiting embodiments thereof, in which:
-
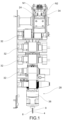
figure 1 shows a schematic view of an air spinning device for implementing a spinning method according to an embodiment of the present invention; -
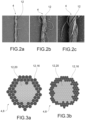
figures 2a, 2b, 2c show a view, with increasing magnifications, of a yarn made with air spinning, of the prior art; -
figures 3a-3b show schematic sectional views of two yarns obtained according to the method of the present invention and according to the teachings of the prior art, respectively. - Elements or parts of elements in common to the embodiments described below are referred to with the same reference numerals.
- With reference to the aforesaid figures,
reference numeral 4 indicates a yarn obtained by means of an air spinning, preferably with multiple feeding. - The present invention finds application in the use on man-made/synthetic fibers and possibly fibers mixed with cotton, but not 100% cotton.
- The
yarn 4 comprises a plurality ofthreads 8 each comprising a plurality offibers 12. - By analyzing the
threads 8 in section, a plurality offibers 12 can be seen which can be divided into external fibers 16 and internal fibers 20. - The internal fibers 20 are those which constitute the core of the
thread 8 in turn surrounded by the external fibers 16. - Advantageously, the present invention provides to obtain
yarns 4 with an overall number offibers 12 lower than 200. - Advantageously, it has been found that it is useful to use thicker fibers as the yarn count decreases, so as to keep the total number of
fibers 12 below 200. - The optimum is to have a number of
fibers 12 sufficient to give substance to thethread 8 but not too high to worsen its technical features. - All this is due to the fact that, in air spinning, there is no real twist as in traditional ring spinning: rather, in air spinning, bundles of fibers are obtained that are wound more or less regularly around a core of "neutral" central fibers, that is, substantially not twisted.
- Therefore in the air spinning it has been verified that the external fibers 16 are twisted, while the internal fibers 20 are neutral as can easily be seen in
figures 2a, 2b and 2c . - Typically, in the solutions of the prior art, a yarn Pes 100% of count Ne20 (295.25 dtex), produced with air spinning machines, has a fiber length of 38mm and a section of 1.3 dtex and contains about 227 fibers.
- A yarn Ne16 (369.1 dtex) of the prior art, with the same raw material, would contain 285 fibers.
- The solution of the present invention provides instead to maintain the
fibers 12 under 200 units (maximum value) and the reason is shown infigures 3a, 3b . - In fact, in air spinning only the outermost fibers 16 are involved in the "twisting" while the central or internal ones 20 remain substantially neutral. This means that the ratio between external fibers 16 and internal fibers 20 must remain high, in order to have a yarn with adequate mechanical features.
- Regardless of the count being worked, it can be said that the number of external fibers that are involved in the twisting always remains the same, which is why the more fibers are in the section, the more unfavorable, that is, low, the ratio between external fibers (twisted) and internal fibers (not twisted).
- In the accompanying
figures (3a, 3b ), a yarn with a count Ne20 (295.25 dtex) is ideally represented, made with 1.5 dtex fibers (figure 3a ) and1 .0 dtex fibers (figure 3b ). It is clearly seen that in the first case (figure 3a ), having fibers of an average greater diameter, the number of external fibers 16 or twisted, which are wound, with respect to the internal ones 20 which remain neutral, is much higher than in the second case (figure 3b ), where the individual fibers 12 (whether they are external fibers 16 or internal fibers 20) have a lower average diameter. - The present invention (
figure 3a ), as the counts decrease, provides to increase the section of thefibers 12 used and therefore reduce the total number thereof, to below 200. - This section increase becomes extremely useful in synthetic fibers where the value of the elongation at break increases with the increase in the section of the fibers, with obvious benefits in the final yarn: more resistance and more elasticity mean greater quality and workability of the same yarn.
- The air spinning method provides the steps of preparing at least one web of textile fibers N1, to be fed by at least one introducer
element 24 upstream of anair spinning device 28. - The web N1 is previously drawn with at least one
drawing device 32, and then, after drawing, said web N1 is fed into aspinning chamber 36 of anair spinning device 28. - Inside the
spinning chamber 36 thefibers 12 are spun by means of jets of compressed air, so as to obtain ayarn 4 comprising internal fibers 20 surrounded by external fibers 16, in which the yarn has an overall count lower than or equal to Ne20 (295.25 dtex) of and greater than or equal to Ne10 (590.5 dtex), and in which the total number of internal and external fibers is less than 200. - In particular, the working pressures, i.e. the jets of compressed air inside the
spinning chamber 36, are between 0.45 and 0.6 MPa, i.e. between 4.5 and 6 bar. - The working speeds of the compressed air leaving the relative jets are comprised between 400 m/min and 500 m/min.
- Obviously, it is possible to feed two or more webs N1, N2, with respective introducer
elements 24, into the air spinning device 28: these webs are joined together inside thespinning chamber 36. - As can be seen from the above description, the air-jet spinning method according to the invention allows the drawbacks of the prior art to be overcome.
- In particular, the present invention allows obtaining, by means of air spinning, yarns with a count lower than or equal to Ne20 (295.25 dtex) and greater than or equal to Ne10 (590.5 dtex). These yarns have features of resistance and elasticity which are superior to the solutions obtainable with the methods of the prior art.
- In fact, as seen, as the counts decrease, it is provided to increase the section of the fibers used and therefore reduce the total number thereof, to a value below 200.
- In this way, increasing the average diameter of the fibers, the number of external fibers, twisted, which are wound, with respect to the internal ones which remain neutral, is much higher: this aspect determines the improvement of the mechanical features of the yarn obtained.
- Moreover, as seen, the section increase becomes extremely useful in synthetic fibers where the value of the elongation at break increases with the increase in the section of the fibers: therefore more resistance and more elasticity are obtained and, consequently, even greater quality and workability of the same yarn.
- Substantially, the present invention goes against the known and consolidated idea in the art of increasing the number of fibers in yarns in order to improve the strength and elasticity of the yarn produced. The present invention teaches exactly the opposite, namely to decrease the number of fibers in the yarns, increasing their average size, in order to improve their mechanical and workability features. Such teaching finds advantageous application in the air-jet spinning sector.
Claims (7)
- Air spinning method comprising the steps of:- preparing at least one web of textile fibers (N1), to be fed by at least one introducer element (24) upstream of an air spinning device (28), said textile fibers being man-made/synthetic fibers and possibly fibers mixed with cotton but not 100% cotton,- drawing said at least one web (N1) with at least one drawing device (32),- feeding said web (N1), previously drawn, in a spinning chamber (36) of the air spinning device (28),- spinning the fibers (12) inside the spinning chamber (36) by means of compressed air jets, so as to:- obtain a yarn (4) comprising internal fibers (20) surrounded by external fibers (16),- wherein the yarn (4) has an overall thread count not exceeding Ne20 (295.25 dtex) and wherein the total number of internal (20) and external (16) fibers is less than 200, determined according to the formula given in the description,- wherein the external fibers(16) are twisted, while the internal fibers (20) are neutral and- wherein the working pressures, i.e. of the compressed air jets inside the spinning chamber (36), are between 0.45 and 0.6 MPa.
- An air spinning method according to claim 1, wherein said overall thread count (4) is greater than or equal to Ne10 (590.5 dtex).
- An air spinning method according to claim 1 or 2, wherein the method comprises the step of increasing the average cross-section or diameter of the fibers (12) of the yarn (4) gradually as the yarn count in Ne of the yarn (4) to be produced decreases, so as to maintain the total number of internal (20) and external (16) fibers below 200, determined according to the formula given in the description.
- Air spinning method according to claim 1, 2 or 3, wherein the method comprises the steps of preparing two textile fibre webs (N1,N2), to be fed by at least one corresponding introducer element (24) upstream of the air spinning device (28), the fibers being man-made/synthetic fibers and possibly fibers mixed with cotton but not 100% cotton,- drawing each of said webs (N1, N2) with at least one drawing device (32),- joining said webs (N1,N2) inside the spinning chamber (36) and spinning the fibers so as to obtain a yarn with a total thread count of less than Ne20 (295.25 dtex) and wherein the total number of internal (20) and external (16) fibers is less than 200, determined according to the formula given in the description.
- Air spinning method according to any one of the preceding claims, wherein the working speeds of the compressed air in output from relative jets, inside the spinning chamber (36), are between 400 m/min and 500 m/min.
- A yarn (4) obtained by means of the air spinning method according to any one of the preceding claims wherein said yarn has an overall thread count of less than Ne20 (295.25 dtex), wherein the total number of inner (20) and outer (16) fibers of the yarn (4) is less than 200, determined according to the formula given in the description, and wherein said fibers are man-made/synthetic fibers and possibly fibers mixed with cotton but not 100% cotton.
- The yarn (4) according to claim 6, wherein said overall thread count is greater than or equal to Ne10 (590.5 dtex).
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| IT102018000010751A IT201800010751A1 (en) | 2018-12-03 | 2018-12-03 | AIR SPINNING METHOD FOR THE PRODUCTION OF BIG YARNS WITH A TITLE LESS THAN Ne20 AND THE RELATIVE YARN |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP3663444A1 EP3663444A1 (en) | 2020-06-10 |
| EP3663444B1 true EP3663444B1 (en) | 2025-04-23 |
Family
ID=65767192
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP19212913.8A Active EP3663444B1 (en) | 2018-12-03 | 2019-12-02 | Air spinning method for the production of large yarns with count lower than ne20 and respective yarn |
Country Status (4)
| Country | Link |
|---|---|
| US (1) | US20200173062A1 (en) |
| EP (1) | EP3663444B1 (en) |
| CN (1) | CN111254528B (en) |
| IT (1) | IT201800010751A1 (en) |
Families Citing this family (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US11359309B2 (en) | 2018-12-21 | 2022-06-14 | Target Brands, Inc. | Ring spun yarn and method |
Family Cites Families (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US5188892A (en) * | 1986-10-31 | 1993-02-23 | E. I. Du Pont De Nemours And Company | Spun textile yarns |
| US6250060B1 (en) * | 1997-04-18 | 2001-06-26 | Wellman, Inc. | Method of producing improved knit fabrics from blended fibers |
| US6146759A (en) * | 1999-09-28 | 2000-11-14 | Land Fabric Corporation | Fire resistant corespun yarn and fabric comprising same |
| CN101294319B (en) * | 2008-05-26 | 2010-06-02 | 东华大学 | Air-jet vortex spinning device with low noil |
| CH709749A1 (en) * | 2014-06-12 | 2015-12-15 | Rieter Ag Maschf | Air-jet spinning machine and method for operating such. |
| JP2018090923A (en) * | 2016-12-01 | 2018-06-14 | 村田機械株式会社 | Spinning machine and spinning method |
| CN106702554B (en) * | 2017-02-28 | 2019-01-25 | 江南大学 | A ring spinning machine with a wetting device for hairiness reduction |
-
2018
- 2018-12-03 IT IT102018000010751A patent/IT201800010751A1/en unknown
-
2019
- 2019-11-29 US US16/699,342 patent/US20200173062A1/en not_active Abandoned
- 2019-12-02 EP EP19212913.8A patent/EP3663444B1/en active Active
- 2019-12-03 CN CN201911219572.8A patent/CN111254528B/en active Active
Non-Patent Citations (2)
| Title |
|---|
| MERTOVÁ IVA ET AL: "Effect of the selected machine variables on the structural characteristics of air-jet spun yarn", THE JOURNAL OF THE TEXTILE INSTITUTE, vol. 111, no. 11, 1 November 2020 (2020-11-01), GB, pages 1556 - 1566, XP093044821, ISSN: 0040-5000, DOI: 10.1080/00405000.2020.1715607 * |
| ZHENG SHAOMING ET AL: "A study of the fiber distribution in yarn cross section for vortex-spun yarn", TEXTILE RESEARCH JOURNAL, vol. 82, no. 15, 3 May 2012 (2012-05-03), GB, pages 1579 - 1586, XP093044830, ISSN: 0040-5175, Retrieved from the Internet <URL:http://journals.sagepub.com/doi/full-xml/10.1177/0040517511431315> DOI: 10.1177/0040517511431315 * |
Also Published As
| Publication number | Publication date |
|---|---|
| US20200173062A1 (en) | 2020-06-04 |
| EP3663444A1 (en) | 2020-06-10 |
| CN111254528A (en) | 2020-06-09 |
| CN111254528B (en) | 2023-07-11 |
| IT201800010751A1 (en) | 2020-06-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP2867393B1 (en) | Core spun elastic composite yarn and woven fabric thereof | |
| CA1043998A (en) | Roving and process for its manufacture | |
| US6405519B1 (en) | Composite, break-resistant sewing thread and method | |
| CN107400947A (en) | The negative poisson's ratio yarn and its composite spinning device of a kind of RING SPINNING, method and purposes | |
| EP1718791B1 (en) | Spun yarn, and method and apparatus for the manufacture thereof | |
| CN101942718A (en) | Elastic blended yarn and preparation method thereof | |
| CN104451917A (en) | Production method for nylon mother yarns | |
| CN112899839A (en) | High-elastic warm-keeping vortex composite spun yarn and production process thereof | |
| KR20180103508A (en) | Process Of Producing Wool-Like Synthetic―Fiber/Cellulose―Fiber Airjet Complex―Yarn Having Excellent Friction Resistance | |
| CN109162000A (en) | A kind of manufacturing method of the low draw ratio brocade ammonia air-coating silk of fine-denier | |
| EP3663444A1 (en) | Air spinning method for the production of large yarns with count lower than ne20 and relative yarn | |
| CN117188004A (en) | A three-component spiral auxetic yarn based on ring spinning and its preparation method | |
| KR102188327B1 (en) | Multi collector for easily manufacturing a variety of spining yarn | |
| CN104593907B (en) | A kind of crush cutting system method of short-staple | |
| JP4594715B2 (en) | Manufacturing method of long and short composite spun yarn | |
| EP1591571A1 (en) | Down branch fiber fabric and the fabricating method thereof | |
| CN101205656A (en) | Device for producing knitting fabric | |
| KR100332037B1 (en) | Spinning method of bulky tube yarn | |
| CN101146938A (en) | Staple yarn manufacturing method | |
| JP4916818B2 (en) | Method for producing double layer yarn | |
| US20250198058A1 (en) | Filamentary core, elastic composite yarn comprising the filamentary core, fabric comprising the filamentary core or the elastic composite yarn and method for manufacturing the filamentary core or the elastic composite yarn | |
| CN101137775A (en) | Melt spinning method for producing composite yarn and composite yarn | |
| JP4099925B2 (en) | Spun yarn and woven / knitted fabric using the same | |
| WO2019038784A1 (en) | Multi-ply separable interlaced yarns, methods for manufacturing thereof and woven textile fabrics thereof | |
| JP2000096401A (en) | Stretchable warp knit |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE APPLICATION HAS BEEN PUBLISHED |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20201203 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20230519 |
|
| P01 | Opt-out of the competence of the unified patent court (upc) registered |
Effective date: 20230526 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| INTG | Intention to grant announced |
Effective date: 20250103 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602019068944 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1787838 Country of ref document: AT Kind code of ref document: T Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250825 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250724 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250723 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250723 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250823 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20251105 Year of fee payment: 7 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20251130 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602019068944 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: L10 Free format text: ST27 STATUS EVENT CODE: U-0-0-L10-L00 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260304 |
|
| 26N | No opposition filed |
Effective date: 20260126 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20251222 Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: H13 Free format text: ST27 STATUS EVENT CODE: U-0-0-H10-H13 (AS PROVIDED BY THE NATIONAL OFFICE) Effective date: 20260723 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20250423 |