EP3511434B1 - Process for producing ls-crnimo30c steel forging using continuous casting billet for subsea oil production wellhead device - Google Patents
Process for producing ls-crnimo30c steel forging using continuous casting billet for subsea oil production wellhead device Download PDFInfo
- Publication number
- EP3511434B1 EP3511434B1 EP17869366.9A EP17869366A EP3511434B1 EP 3511434 B1 EP3511434 B1 EP 3511434B1 EP 17869366 A EP17869366 A EP 17869366A EP 3511434 B1 EP3511434 B1 EP 3511434B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- steel
- billet
- forged
- continuous casting
- forging
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images
Classifications
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C33/00—Making ferrous alloys
- C22C33/04—Making ferrous alloys by melting
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/001—Continuous casting of metals, i.e. casting in indefinite lengths of specific alloys
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B22—CASTING; POWDER METALLURGY
- B22D—CASTING OF METALS; CASTING OF OTHER SUBSTANCES BY THE SAME PROCESSES OR DEVICES
- B22D11/00—Continuous casting of metals, i.e. casting in indefinite lengths
- B22D11/10—Supplying or treating molten metal
- B22D11/11—Treating the molten metal
- B22D11/114—Treating the molten metal by using agitating or vibrating means
- B22D11/115—Treating the molten metal by using agitating or vibrating means by using magnetic fields
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D1/00—General methods or devices for heat treatment, e.g. annealing, hardening, quenching or tempering
- C21D1/26—Methods of annealing
- C21D1/30—Stress-relieving
-
- C—CHEMISTRY; METALLURGY
- C21—METALLURGY OF IRON
- C21D—MODIFYING THE PHYSICAL STRUCTURE OF FERROUS METALS; GENERAL DEVICES FOR HEAT TREATMENT OF FERROUS OR NON-FERROUS METALS OR ALLOYS; MAKING METAL MALLEABLE, e.g. BY DECARBURISATION OR TEMPERING
- C21D8/00—Modifying the physical properties of ferrous metals or ferrous alloys by deformation combined with, or followed by, heat treatment
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/02—Ferrous alloys, e.g. steel alloys containing silicon
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/04—Ferrous alloys, e.g. steel alloys containing manganese
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/12—Ferrous alloys, e.g. steel alloys containing tungsten, tantalum, molybdenum, vanadium, or niobium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/44—Ferrous alloys, e.g. steel alloys containing chromium with nickel with molybdenum or tungsten
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/46—Ferrous alloys, e.g. steel alloys containing chromium with nickel with vanadium
-
- C—CHEMISTRY; METALLURGY
- C22—METALLURGY; FERROUS OR NON-FERROUS ALLOYS; TREATMENT OF ALLOYS OR NON-FERROUS METALS
- C22C—ALLOYS
- C22C38/00—Ferrous alloys, e.g. steel alloys
- C22C38/18—Ferrous alloys, e.g. steel alloys containing chromium
- C22C38/40—Ferrous alloys, e.g. steel alloys containing chromium with nickel
- C22C38/48—Ferrous alloys, e.g. steel alloys containing chromium with nickel with niobium or tantalum
Definitions
- the present invention relates to a field of manufacturing forged steel, specially relates to a process for manufacturing CrNiMo30C forged steel for a wellhead device of deep-sea oil extraction by continuous casting.
- the wellhead device of deep-sea oil extraction consists of casing-head, tubing-head and production tree, and is an important device for producing gas-oil.
- the wellhead device is mainly used to control the pressure of production wellhead and to regulate the flow rate of oil (gas) and water wells, how good the performance is relates to whether the oil/gas wells can produce safely and efficiently or not.
- the wellhead device of deep-sea oil extraction is usually forged by mold casting ingot, because the inner quality of steel ingot in manufacturing is better than that of continuous casting billet (especially the alloy containing a certain amount of Cr, Ni, Mo etc.), the forged bar can meet the higher requirements of ultrasonic flaw detection and mechanical property required by the wellhead device of deep-sea oil extraction. While the casting and solidification process of molten steel of continuous casting billet is different from those of mold casting ingot, the inner quality of continuous casing billet has problems of bad compactness and heavy segregation, therefore, the forged bar by continuous casting billet usually can not meet the requirements of use in the wellhead device of deep-sea oil extraction.
- each forged bar by mold casting ingot has to be cut in heads and tails, the production ratio in forging is only about 80%, whereas the forged bar by continuous casting billet is poured at one time with several stoves of steel. Because the billet yield in continuous casting is high, the production ratio in forging is up to 90% or more, the production efficiency is high and the cost is low. Thus, improving the inner quality of continuous casting billets, controlling the process of forging, and replacing the mold casting ingots by continuous casting billets for manufacturing the wellhead device of deep-sea oil extraction would be a better development tendency.
- CN106591680A discloses a technology for producing an LS-CrNiMo30C steel for a subsea oil production wellhead device, using a continuous casting billet.
- the technology comprises the steps of smelting molten steel, continuously casting, forging, annealing, cooling, etc.; the heating speed is equal to or less than 200°C per hour, the heating temperature of forging is 1200-1250°C, ensuring that the billet is completely heated, the initial forging temperature is higher than 1150°C, and the final forging temperature is not lower than 850°C; after leaving the production line, the forged steel is at a high temperature of equal to or greater than 500°C, and is then slowly cooled in sand; after the temperature drops to 200°C or lower, the forged steel is taken out of pit and slowly cooled.
- the object of the present invention is, by improving the inner quality of continuous casting of ⁇ 600mm CrNiMo30C steel and by adopting a reasonable forging process, to manufacture forged round steel of ⁇ 300-400mm via replacing mold casting ingot with continuous casting billet.
- the inner quality meets requirements of an ultrasonic test according to grade D/d of SEP 1921 standard and a mechanical property test according to APISPEC 6A standard.
- the present invention provides a process for manufacturing CrNiMo30C forged steel as described in our claim 1.
- the advantages of the present invention focus on: Compared with the prior process of manufacturing CrNiMo30C forged steel by mold casting ingot, the present invention has good benefits:
- the present invention further describes a process for manufacturing CrNiMo30C forged steel for a wellhead device of deep-sea oil extraction by continuous casting billet in detail with reference to embodiments.
- Chemical constituents of CrNiMo30C steel are as follows: C: 0.25 ⁇ 0.40%, Si: 0.15 ⁇ 0.40%, Mn: 0.80 ⁇ 1.30%, P: ⁇ 0.010%, S: ⁇ 0.008%, Cr: 0.85 ⁇ 1.55%, Mo: 0.30 ⁇ 0.65%, Ni: 0.80 ⁇ 1.40%, V: 0.02 ⁇ 0.08%, Nb: 0.02 ⁇ 0.05%, Cu ⁇ 0.25%, B ⁇ 0.0005%, H ⁇ 0.0002%, the balance is Fe and the unavoidable impurity elements.
- the steel is selected to be CrNiMo30C steel
- the steel is selected to be CrNiMo30C steel.
Landscapes
- Chemical & Material Sciences (AREA)
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Materials Engineering (AREA)
- Metallurgy (AREA)
- Organic Chemistry (AREA)
- Thermal Sciences (AREA)
- Physics & Mathematics (AREA)
- Crystallography & Structural Chemistry (AREA)
- Child & Adolescent Psychology (AREA)
- Health & Medical Sciences (AREA)
- Forging (AREA)
- Continuous Casting (AREA)
- Heat Treatment Of Steel (AREA)
Description
- The present invention relates to a field of manufacturing forged steel, specially relates to a process for manufacturing CrNiMo30C forged steel for a wellhead device of deep-sea oil extraction by continuous casting.
- The wellhead device of deep-sea oil extraction consists of casing-head, tubing-head and production tree, and is an important device for producing gas-oil. The wellhead device is mainly used to control the pressure of production wellhead and to regulate the flow rate of oil (gas) and water wells, how good the performance is relates to whether the oil/gas wells can produce safely and efficiently or not.
- At present the wellhead device of deep-sea oil extraction is usually forged by mold casting ingot, because the inner quality of steel ingot in manufacturing is better than that of continuous casting billet (especially the alloy containing a certain amount of Cr, Ni, Mo etc.), the forged bar can meet the higher requirements of ultrasonic flaw detection and mechanical property required by the wellhead device of deep-sea oil extraction. While the casting and solidification process of molten steel of continuous casting billet is different from those of mold casting ingot, the inner quality of continuous casing billet has problems of bad compactness and heavy segregation, therefore, the forged bar by continuous casting billet usually can not meet the requirements of use in the wellhead device of deep-sea oil extraction. However, each forged bar by mold casting ingot has to be cut in heads and tails, the production ratio in forging is only about 80%, whereas the forged bar by continuous casting billet is poured at one time with several stoves of steel. Because the billet yield in continuous casting is high, the production ratio in forging is up to 90% or more, the production efficiency is high and the cost is low. Thus, improving the inner quality of continuous casting billets, controlling the process of forging, and replacing the mold casting ingots by continuous casting billets for manufacturing the wellhead device of deep-sea oil extraction would be a better development tendency.
-
CN106591680A discloses a technology for producing an LS-CrNiMo30C steel for a subsea oil production wellhead device, using a continuous casting billet. The technology comprises the steps of smelting molten steel, continuously casting, forging, annealing, cooling, etc.; the heating speed is equal to or less than 200°C per hour, the heating temperature of forging is 1200-1250°C, ensuring that the billet is completely heated, the initial forging temperature is higher than 1150°C, and the final forging temperature is not lower than 850°C; after leaving the production line, the forged steel is at a high temperature of equal to or greater than 500°C, and is then slowly cooled in sand; after the temperature drops to 200°C or lower, the forged steel is taken out of pit and slowly cooled. - Aiming at above prior arts, the object of the present invention is, by improving the inner quality of continuous casting of Φ600mm CrNiMo30C steel and by adopting a reasonable forging process, to manufacture forged round steel of Φ300-400mm via replacing mold casting ingot with continuous casting billet. The inner quality meets requirements of an ultrasonic test according to grade D/d of SEP 1921 standard and a mechanical property test according to APISPEC 6A standard.
- The present invention provides a process for manufacturing CrNiMo30C forged steel as described in our claim 1.
- Specifically, it relates to a process for manufacturing CrNiMo30C forged steel for a wellhead device of deep-sea oil extraction, by continuous casting, including the following steps
- 1) Smelting molten steel: CrNiMo30C steel of a medium-carbon low-alloy CrNoMo steel, its constituents and mass percentages are as follows: C: 0.25∼0.40%, Si: 0.15∼0.40%, Mn: 0.80∼1.30%, P: ≤0.010%, S: ≤0.008%, Cr: 0.85∼1.55%, Mo: 0.30∼0.65%, Ni: 0.80∼ 1.40%, V: 0.02∼0.08%, Nb: 0.02∼0.05%, Cu ≤0.25%, B ≤0.0005%, H ≤0.0002%, the balance is Fe and the unavoidable impurity elements, the molten steel is processed by KR pretreatment, BOF converter smelting, LF refining and RH vacuum degassing, thereby the CrNiMo30C steel with low H, S and P is obtained, and the steel is finally controlled according the requirements of P ≤0.010%, S ≤0.005% and H ≤1.5ppm;
- 2) Continuous casting: the molten steel is further processed by argon protection, mixed electromagnetic stirring with mold electromagnetic stirring (M-EMS) and final electromagnetic stirring (F-EMS), in cooperation with secondary cooling water and low speed casting, and strictly controlling a superheat degree of 20-35°C, thereby to decrease columnar crystals and enlarge equiaxed crystal, to prevent the development of columnar crystals to refine grains, to reduce segregation degree in steel crystallization process, to sufficiently ensure uniformity and compactness of inner structure; a continuous casting billet of Φ600mm leaves the production line and is delivered to a slow cooling pit at a high temperature of equal to or more than 500°C, and is kept warm for equal to or more than 36h in the pit, and then the continuous billet is timely forged after outside the pit; the macrostructure of the continuous casting billet meets the requirements of appendix A of YB/T4149 standard: center porosity is equal to or less than grade 2.0, center crack is equal to or less than grade 1.0, shrinkage cavity is equal to or less than grade 1.0, defects of intermediate cracks, white flakes and upwarping defects are forbidden;
- 3) Forging: the billet is heated and the heating speed is equal to or less than 200°C per hour, the heating temperature of forging is 1200-1250°C, ensuring that the billet is completely heated, the initial forging temperature is higher than 1150°C, and the final forging temperature is not lower than 850°C, the continuous casting billet is freely forged by a 1400T double-station hydraulic machine, oxide coating of the continuous billet is timely removed during forging, the billet is drawn into square shape by a small reduction amount of 20-30mm at initial cogging, thereby to prevent surface cracks, and is drawn into square shape by a large reduction amount of 70-80mm at intermediate cogging, thereby to penetrate the forging force into the core so as to improve the inner quality, and the billet is further drawn and its outside shaped as a circle, and is finally finished to a finished size; after leaving the production line, the forged steel is at a high temperature of equal to or greater than 500°C and is then slowly cooled in sand; after the temperature drops to 200°C or lower, the forged steel is taken out of the pit and slowly cooled;
- 4) Performing stress relief annealing treatment on forged steel: the annealing temperature is 650-700°C, keeping warm for 12 hours or more, cooling to below 300°C along with the furnace, taking the forged billet outside the furnace, and air-cooling to room temperature;
- 5) Inspection: cutting head and tail parts of each piece of forged steel, and performing an ultrasonic test according to grade D/d of SEP 1921 standard to each piece of steel; performing a mechanical property test to a batch of the steel, wherein the tensile, the impact and the hardness should meet the requirements of APISPEC 6A standard.
- Compared with the prior art, the advantages of the present invention focus on:
Compared with the prior process of manufacturing CrNiMo30C forged steel by mold casting ingot, the present invention has good benefits: - Using "KR-BOF-LF-RH-CCM" in smelting and continuous casting, so that the degree of automation and mechanization is high, operating condition is therefore improved, and the production efficiency is improved.
- Using mixed electromagnetic stirring with mold electromagnetic stirring (M-EMS) and final electromagnetic stirring (F-EMS), to improve the inner quality of continuous quality; controlling forging heating process and the reduction amount at cogging, to obtain a forged bar of Cr, Ni, Mo with good inner quality for use in a wellhead device of deep-sea oil extraction; replacing casting ingot by continuous casting, so that the yield ratio is improved, and the cost advantage is significant.
-
-
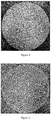
Figure 1 illustrates macrostructure of Φ350mm forged round steel by continuous casting billet in embodiment 1; -
Figure 2 illustrates macrostructure of Φ390mm forged round steel by continuous casting billet in embodiment 2. - The present invention further describes a process for manufacturing CrNiMo30C forged steel for a wellhead device of deep-sea oil extraction by continuous casting billet in detail with reference to embodiments.
- Chemical constituents of CrNiMo30C steel are as follows: C: 0.25∼0.40%, Si: 0.15∼ 0.40%, Mn: 0.80∼1.30%, P: ≤0.010%, S: ≤0.008%, Cr: 0.85∼1.55%, Mo: 0.30∼0.65%, Ni: 0.80∼1.40%, V: 0.02∼0.08%, Nb: 0.02∼0.05%, Cu ≤0.25%, B ≤0.0005%, H ≤0.0002%, the balance is Fe and the unavoidable impurity elements.
- The steel is selected to be CrNiMo30C steel;
- 1) Smelting:
- the molten steel is processed by KR pretreatment to perform desulphurization and desilicication,
- before the molten steel is delivered into converter, S=0.005%,
- BOF converter smelting mainly performs dephosphorizing, decarbonizing and heating, alloy metal is added after tapping.
After degassing in RH vacuum and after breaking the vacuum, H is determined to be H=0.8ppm. - 2) Continuous casting:
the molten steel is further processed by argon protection, the superheat degree is controlled to be 25°C, a continuous casting billet of Φ600mm is produced by mixed electromagnetic stirring with mold electromagnetic stirring (M-EMS) and final electromagnetic stirring (F-EMS), and then it leaves the production line and is delivered to a slow cooling pit at 550°C, and is kept warm for 36h in the pit, then the continuous billet is taken outside the pit and the macrostructure is tested according to appendix A of YB/T4149 standard: center porosity is grade 1.0, center crack is grade 0, shrinkage cavity is grade 0, free of intermediate cracks, white flakes or upwarping defects, etc. - 3) Forging:
the continuous casting billet of Φ600mm is cold delivered to the furnace and is heated to 1200°C, the heating speed is equal to or less than 200°C per hour, and is kept warm for 5 hours, the initial forging temperature is 1150°C, and the final forging temperature is not lower than 850°C, the continuous casting billet is freely forged by a 1400T double-station hydraulic machine, oxide coating of the continuous billet is timely removed during forging, the billet is drawn into about 550mm square by a small reduction amount of 20-30mm at initial cogging, and the billet is drawn into about 400mm square by a large reduction amount of 70-80mm at intermedia cogging, thereby to penetrate the forging force into the core, so as to improve the inner quality, and the billet is further drawn and its outside is shaped as a circle of Φ370mm, and is finally finished to a finished circle of Φ350mm; after leaving the production line, the forged steel is air-cooled to 550°C and then is slowly cooled in sand; after the temperature drops to 200°C or lower, the forged steel is taken out of the pit. - 4) Annealing:
after the forged steel is taken out of the pit, performing stress relief annealing treatment, the annealing temperature is 660°C, keeping warm for 12 hours or more, cooling to below 300°C along with the furnace, taking the forged billet outside the furnace, and air-cooling to room temperature, the tested macrostructure is shown infigure 1 . - 5) Inspection:
cutting head and tail parts of each piece of forged steel, and performing an ultrasonic test according to grade D/d of SEP 1921 standard to each piece of steel; performing a mechanical property test to a batch of the steel, wherein the tensile, the impact and the hardness meet the requirements of APISPEC 6A standard. - The steel is selected to be CrNiMo30C steel.
- 1) Smelting:
- the molten steel is processed by KR pretreatment to perform desulphurization and desilicication,
- before the molten steel is delivered into converter, S=0.003%,
- BOF converter smelting mainly performs dephosphorizing, decarbonizing and heating, alloy metal is added after tapping.
After degassing in RH vacuum and after breaking the vacuum, H is determined to be H=1.0ppm. - 2) Continuous casting:
the molten steel is further processed by argon protection, the superheat degree is controlled to be 27°C, a continuous casting billet of Φ600mm is produced by mixed electromagnetic stirring with mold electromagnetic stirring (M-EMS) and final electromagnetic stirring (F-EMS), and then it leaves the production line and is delivered to a slow cooling pit at 580°C, and is kept warm for 40h in the pit, after slowly cooling the continuous billet is taken outside the pit and the macrostructure is tested according to appendix A of YB/T4149 standard: center porosity is grade 1.5, center crack is grade 0.5, shrinkage cavity is grade 0, free of intermediate cracks, white flakes or upwarping defects, etc.. - 3) Forging:
the continuous casting billet of Φ600mm is cold delivered to the furnace and is heated to 1220°C, the heating speed is equal to or less than 200°C per hour, and is kept warm for 5 hours, the initial forging temperature is 1120°C, and the final forging temperature is not lower than 850°C, the continuous casting billet is freely forged by a 1400T double-station hydraulic machine, oxide coating of the continuous billet is timely removed during forging, the billet is drawn into about 550mm square by a small reduction amount of 20-30mm at initial cogging, and the billet is drawn into about 410mm square by a large reduction amount of 70-80mm at intermedia cogging, thereby to penetrate the forging force into the core so as to improve the inner quality, and the billet is further drawn and its outside shaped as a circle of Φ400mm, and is finally finished to a finished circle of Φ390mm; after leaving the production line, the forged steel is air-cooled to 550°C and then is slowly cooled in sand; after the temperature drops to 200°C or lower, the forged steel is taken out of the pit. - 4) Annealing:
after the forged steel is taken out of the pit, performing stress relief annealing treatment, the annealing temperature is 660°C, keeping warm for 12 hours or more, cooling to below 300°C along with the furnace, taking the forged billet outside the furnace, and air-cooling to room temperature, the tested macrostructure is shown infigure 2 ; - 5) Inspection:
cutting head and tail parts of each piece of forged steel, and performing an ultrasonic test according to grade D/d of SEP 1921 standard to each piece of steel; performing a mechanical property test to a batch of the steel, wherein the tensile, the impact and the hardness meet the requirements of APISPEC 6A standard.
Claims (1)
- A process for manufacturing CrNiMo30C forged steel for a wellhead device of deep-sea oil extraction, by continuous casting, characterized in including the following steps1) Smelting molten steel: CrNiMo30C steel of a medium-carbon low-alloy CrNoMo steel, its constituents and mass percentages are as follows: C: 0.25∼0.40%, Si: 0.15∼0.40%, Mn: 0.80∼1.30%, P: ≤0.010%, S: ≤0.008%, Cr: 0.85∼1.55%, Mo: 0.30∼0.65%, Ni: 0.80∼ 1.40%, V: 0.02∼0.08%, Nb: 0.02∼0.05%, Cu ≤0.25%, B ≤0.0005%, H ≤0.0002%, the balance is Fe and the unavoidable impurity elements,
wherein the molten steel is processed by Kanbara Reactor KR pretreatment, dephosphorizing and decarbonizing in Basic Oxygen Furnace BOF converter smelting and heating, adding alloy after tapping, Ladle Furnace LF refining and Ruhrstahl Heraeus RH vacuum degassing, thereby the CrNiMo30C steel with low H, S and P is obtained, and the steel is finally controlled according the requirements of P ≤0.010%, S ≤0.005% and H ≤1.5ppm;2) Continuous casting: the molten steel is further processed by argon protection, mixed electromagnetic stirring with mold electromagnetic stirring (M-EMS) and final electromagnetic stirring (F-EMS), in cooperation with secondary cooling water and low speed casting, and strictly controlling a superheat degree of 20-35°C, thereby to decrease columnar crystals and enlarge equiaxed crystal, to prevent the development of columnar crystals to refine grains, to reduce segregation degree in steel crystallization process, to sufficiently ensure uniformity and compactness of inner structure; a continuous casting billet of Φ600mm leaves the production line and is delivered to a slow cooling pit at a high temperature of equal to or more than 500°C, and is kept warm for equal to or more than 36h in the pit, and then the continuous billet is timely forged after outside the pit; the macrostructure of the continuous casting billet meets the requirements of appendix A of YB/T4149-2006 standard: center porosity is equal to or less than grade 2.0, center crack is equal to or less than grade 1.0, shrinkage cavity is equal to or less than grade 1.0, defects of intermediate cracks, white flakes and upwarping defects are forbidden;3) Forging: the billet is heated and the heating speed is equal to or less than 200°C per hour, the heating temperature of forging is 1200-1250°C, ensuring that the billet is completely heated, the initial forging temperature is higher than 1150°C, and the final forging temperature is not lower than 850°C, the continuous casting billet is freely forged by a 1400T double-station hydraulic machine, oxide coating of the continuous billet is timely removed during forging, the billet is drawn into square shape by a small reduction amount of 20-30mm at initial cogging, thereby to prevent surface cracks, and is drawn into square shape by a large reduction amount of 70-80mm at intermediate cogging, thereby to penetrate the forging force into the core so as to improve the inner quality, and the billet is further drawn and its outside shaped as a circle, and is finally finished to a finished size; after leaving the production line, the forged steel is at a high temperature of equal to or greater than 500°C, and is then slowly cooled in sand; after the temperature drops to 200°C or lower, the forged steel is taken out of pit and slowly cooled ;4) Performing stress relief annealing treatment on forged steel: the annealing temperature is 650-700°C, keeping warm for 12 hours or more, cooling to below 300°C along with the furnace, taking the forged billet outside the furnace, and air-cooling to room temperature.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201610984844.3A CN106591680B (en) | 2016-11-09 | 2016-11-09 | A kind of technique of continuous casting billet production deep-sea wellhead for production CrNiMo30C steel forging materials |
| PCT/CN2017/096706 WO2018086394A1 (en) | 2016-11-09 | 2017-08-10 | Process for producing ls-crnimo30c steel forging using continuous casting billet for subsea oil production wellhead device |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP3511434A1 EP3511434A1 (en) | 2019-07-17 |
| EP3511434A4 EP3511434A4 (en) | 2020-03-18 |
| EP3511434B1 true EP3511434B1 (en) | 2021-09-29 |
Family
ID=58590797
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP17869366.9A Active EP3511434B1 (en) | 2016-11-09 | 2017-08-10 | Process for producing ls-crnimo30c steel forging using continuous casting billet for subsea oil production wellhead device |
Country Status (3)
| Country | Link |
|---|---|
| EP (1) | EP3511434B1 (en) |
| CN (1) | CN106591680B (en) |
| WO (1) | WO2018086394A1 (en) |
Families Citing this family (25)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN106591680B (en) * | 2016-11-09 | 2018-02-23 | 江阴兴澄特种钢铁有限公司 | A kind of technique of continuous casting billet production deep-sea wellhead for production CrNiMo30C steel forging materials |
| CN110284057B (en) * | 2019-06-18 | 2022-02-15 | 江阴兴澄特种钢铁有限公司 | High-strength long-life gear steel |
| CN110616360A (en) * | 2019-09-28 | 2019-12-27 | 江苏联峰能源装备有限公司 | Production method of 32Cr3Mo1V continuous casting round billet for roll sleeve |
| CN110899330B (en) * | 2019-10-29 | 2021-09-10 | 邯郸钢铁集团有限责任公司 | Center crack control process for large-size 42CrMo round steel with thickness of more than 70mm |
| CN112029974B (en) * | 2020-08-21 | 2022-05-17 | 大冶特殊钢有限公司 | Production process for improving flaw detection qualification rate of 27SiMn large-section forged material |
| CN112251574B (en) * | 2020-08-31 | 2022-04-22 | 伊莱特能源装备股份有限公司 | Manufacturing method of high-performance forged ring for tank car |
| CN114618971B (en) * | 2020-12-10 | 2024-03-12 | 山西宝龙达锻造股份有限公司 | Forging process of duplex stainless steel F55 |
| CN113025878B (en) * | 2021-01-29 | 2022-07-29 | 江阴兴澄特种钢铁有限公司 | Quenching and tempering round steel for oil-well low-alloy well completion tool and manufacturing method thereof |
| CN113046635B (en) * | 2021-03-05 | 2022-07-26 | 天津理工大学 | High-strength and high-toughness corrosion-resistant steel for ocean engineering and manufacturing method thereof |
| CN113481427B (en) * | 2021-04-13 | 2022-06-03 | 江阴兴澄特种钢铁有限公司 | Medium-carbon low-alloy CrMnSiB series steel forging and rolling bar for producing cold heading module by continuous casting billet and manufacturing method thereof |
| CN113523166A (en) * | 2021-07-21 | 2021-10-22 | 苏州雷格姆海洋石油设备科技有限公司 | Production process of 25% Cr large-wall-thickness super binocular stainless steel forging for deep sea connector |
| CN113957206A (en) * | 2021-10-08 | 2022-01-21 | 南京钢铁集团冶金铸造有限公司 | Black skin quenching and tempering process for preparing CrNiMo alloy steel forging circle |
| CN114210893B (en) * | 2021-12-09 | 2023-07-14 | 山西太钢不锈钢股份有限公司 | A kind of manufacturing method of large-diameter stainless steel circular tube billet |
| CN114682723A (en) * | 2022-04-08 | 2022-07-01 | 建龙北满特殊钢有限责任公司 | A kind of manufacturing method of small forging ratio carbon-manganese steel forging material |
| CN115125457B (en) * | 2022-05-26 | 2023-06-16 | 江阴兴澄特种钢铁有限公司 | Steel for-50 ℃ low-temperature-resistant petrochemical heat exchanger tube plate produced by continuous casting large round billets and manufacturing method thereof |
| CN115301908A (en) * | 2022-08-11 | 2022-11-08 | 包头钢铁(集团)有限责任公司 | Method for improving internal structure of round billet by adopting tail end electromagnetic stirring |
| CN115747630B (en) * | 2022-08-30 | 2023-09-12 | 张家港海锅新能源装备股份有限公司 | Steel for deep sea oil extraction equipment pipeline connector and forging method thereof |
| CN115537639A (en) * | 2022-09-20 | 2022-12-30 | 苏州雷格姆海洋石油设备科技有限公司 | Method for manufacturing high-precision parts of control module of deep-sea Christmas tree |
| CN115287548B (en) * | 2022-10-10 | 2023-01-17 | 山东瑞泰新材料科技有限公司 | High expansion alloy steel and its preparation method and application |
| CN116219273B (en) * | 2022-11-22 | 2024-11-29 | 江阴兴澄特种钢铁有限公司 | Drilling pump valve steel of ocean drilling platform and manufacturing method thereof |
| CN115838899B (en) * | 2022-11-22 | 2024-03-01 | 石钢京诚装备技术有限公司 | Ultrahigh-pressure wellhead steel and production method thereof |
| CN116083816A (en) * | 2023-01-09 | 2023-05-09 | 江苏沙钢集团淮钢特钢股份有限公司 | Steel for high-hardenability oversized petroleum equipment and production process thereof |
| CN117444112A (en) * | 2023-10-25 | 2024-01-26 | 芜湖新兴铸管有限责任公司 | A kind of 38CrMoAl continuous casting billet and its forging method |
| CN117448691A (en) * | 2023-12-12 | 2024-01-26 | 江苏沙钢集团淮钢特钢股份有限公司 | Corrosion-resistant, large-sized steel for oil collection equipment and manufacturing method thereof |
| CN118207397A (en) * | 2023-12-25 | 2024-06-18 | 张家港海锅新能源装备股份有限公司 | Production process of F60/F65 forgings for deep-sea oil and gas equipment pipe joints |
Family Cites Families (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| JP2002309350A (en) * | 2001-04-11 | 2002-10-23 | Daido Steel Co Ltd | Roll material for continuous casting |
| JP4626092B2 (en) * | 2001-06-01 | 2011-02-02 | 大同特殊鋼株式会社 | Steel for plastic molds |
| ES2572612T3 (en) * | 2007-03-29 | 2016-06-01 | Kabushiki Kaisha Kobe Seiko Sho | Steel ingot for forging and integral crankshaft |
| CN101279360B (en) * | 2008-05-15 | 2010-09-29 | 天津钢管集团股份有限公司 | Production method of low-alloy steel continuous casting round tube blank with diameter of Ф350~Ф400mm |
| CN102337481B (en) * | 2010-07-20 | 2013-11-13 | 宝山钢铁股份有限公司 | Molybdenum-containing nickel-saving austenitic stainless steel with excellent corrosion resistance and manufacturing method thereof |
| CN102728756B (en) * | 2012-06-27 | 2014-12-17 | 江苏金源锻造股份有限公司 | Wind power spindle flange upsetting process |
| WO2014034658A1 (en) * | 2012-08-29 | 2014-03-06 | 新日鐵住金株式会社 | Electromagnetic stirring apparatus, and continuous casting method |
| CN104894487B (en) * | 2015-06-25 | 2017-02-22 | 江苏沙钢集团淮钢特钢股份有限公司 | High-strength high-toughness steel for valves of oil drilling platforms and technology for manufacturing high-strength high-toughness steel |
| CN104975235A (en) * | 2015-07-20 | 2015-10-14 | 江阴兴澄特种钢铁有限公司 | High-toughness medium-carbon quenched and tempered round steel of grade 120 KSI and manufacturing method thereof |
| CN105624540A (en) * | 2016-03-23 | 2016-06-01 | 攀钢集团攀枝花钢铁研究院有限公司 | Control method of equiaxial crystal ratio of 30CrMo round pipe billet and steel casting blank |
| CN106591680B (en) * | 2016-11-09 | 2018-02-23 | 江阴兴澄特种钢铁有限公司 | A kind of technique of continuous casting billet production deep-sea wellhead for production CrNiMo30C steel forging materials |
-
2016
- 2016-11-09 CN CN201610984844.3A patent/CN106591680B/en active Active
-
2017
- 2017-08-10 WO PCT/CN2017/096706 patent/WO2018086394A1/en not_active Ceased
- 2017-08-10 EP EP17869366.9A patent/EP3511434B1/en active Active
Also Published As
| Publication number | Publication date |
|---|---|
| WO2018086394A1 (en) | 2018-05-17 |
| EP3511434A1 (en) | 2019-07-17 |
| CN106591680B (en) | 2018-02-23 |
| EP3511434A4 (en) | 2020-03-18 |
| CN106591680A (en) | 2017-04-26 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP3511434A1 (en) | Process for producing ls-crnimo30c steel forging using continuous casting billet for subsea oil production wellhead device | |
| CN110157988B (en) | A kind of high-purity, homogeneous rare earth cold roll steel alloy material and preparation method | |
| CN102837165B (en) | Manufacturing method for final-stage driving gear of high-power coal mining machine | |
| CN108220766B (en) | Cr-V hot work die steel and preparation method thereof | |
| CN113481427B (en) | Medium-carbon low-alloy CrMnSiB series steel forging and rolling bar for producing cold heading module by continuous casting billet and manufacturing method thereof | |
| CN102363869B (en) | Manufacturing method of free-cutting ferritic stainless steel 430FM | |
| CN103320727A (en) | Aluminum alloy medium plate preparation method | |
| CN114540699A (en) | High-performance hot-work die steel and preparation method thereof | |
| CN113046641B (en) | A kind of low vanadium nitrogen-containing hot work die steel and preparation method thereof | |
| CN106544594A (en) | Carbon vanadium steel and preparation method thereof in a kind of drill steel | |
| CN112708829A (en) | Preparation method of high-performance steel for transmission shaft of coal mining machine | |
| CN115896634B (en) | High-temperature-resistant nonferrous metal die-casting forming die steel material and preparation method thereof | |
| CN114892106A (en) | Martensite precipitation hardening stainless steel for fracturing pump valve box and short-flow production method of fracturing pump valve box | |
| CN112322868A (en) | High-alloy tool and die steel and preparation method thereof | |
| CN114807558B (en) | A production method of EX50V round steel for mining drill bits | |
| CN113444978A (en) | Preparation method of ultrahigh-strength steel | |
| CN105803152B (en) | The center porosity control method of 30CrMo circular pipe blank steel strands | |
| WO2024087788A1 (en) | Steel for forged bucket teeth of excavator, and preparation method therefor | |
| CN110576163B (en) | Method for producing high-carbon manganese-chromium steel by large-section continuous casting round billet | |
| CN105772666B (en) | The center segregation control method of 30CrMo circular pipe blank steel strands | |
| CN101962737A (en) | Multi-element alloyed ultrahigh-strength sucker rod steel and manufacturing method thereof | |
| CN108015255B (en) | A kind of preparation method of high-speed tool steel | |
| CN112501382B (en) | Preparation method of carbon tool steel for obtaining low-net-shaped carbide | |
| CN104328260B (en) | A kind of method for solving ferrite stainless billet transverse fissure | |
| CN118086769A (en) | Economical steel for saw blade substrate and production method |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE INTERNATIONAL PUBLICATION HAS BEEN MADE |
|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: REQUEST FOR EXAMINATION WAS MADE |
|
| 17P | Request for examination filed |
Effective date: 20190409 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: BA ME |
|
| DAV | Request for validation of the european patent (deleted) | ||
| DAX | Request for extension of the european patent (deleted) | ||
| A4 | Supplementary search report drawn up and despatched |
Effective date: 20200214 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: C22C 38/48 20060101ALI20200210BHEP Ipc: C21D 1/30 20060101ALI20200210BHEP Ipc: C22C 33/04 20060101AFI20200210BHEP Ipc: C22C 38/46 20060101ALI20200210BHEP Ipc: C22C 38/04 20060101ALI20200210BHEP Ipc: C22C 38/18 20060101ALI20200210BHEP Ipc: C22C 38/44 20060101ALI20200210BHEP Ipc: C21D 8/00 20060101ALI20200210BHEP Ipc: C22C 38/12 20060101ALI20200210BHEP Ipc: C22C 38/02 20060101ALI20200210BHEP |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: ZHU, GUORONG Inventor name: HUANG, ZHEN Inventor name: XU, XIAOHONG Inventor name: SHAO, SHUYAN Inventor name: HU, SHAOXIN Inventor name: ZHANG, KUI Inventor name: JI, LING Inventor name: NIE, AICHEN Inventor name: LI, YUN |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: EXAMINATION IS IN PROGRESS |
|
| 17Q | First examination report despatched |
Effective date: 20200430 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: GRANT OF PATENT IS INTENDED |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| RIC1 | Information provided on ipc code assigned before grant |
Ipc: B22D 11/00 20060101ALI20210604BHEP Ipc: C21D 8/00 20060101ALI20210604BHEP Ipc: C21D 1/30 20060101ALI20210604BHEP Ipc: C22C 38/48 20060101ALI20210604BHEP Ipc: C22C 38/46 20060101ALI20210604BHEP Ipc: C22C 38/44 20060101ALI20210604BHEP Ipc: C22C 38/12 20060101ALI20210604BHEP Ipc: C22C 38/18 20060101ALI20210604BHEP Ipc: C22C 38/04 20060101ALI20210604BHEP Ipc: C22C 38/02 20060101ALI20210604BHEP Ipc: C22C 33/04 20060101AFI20210604BHEP |
|
| INTG | Intention to grant announced |
Effective date: 20210624 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: THE PATENT HAS BEEN GRANTED |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AL AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO RS SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP Ref country code: AT Ref legal event code: REF Ref document number: 1434249 Country of ref document: AT Kind code of ref document: T Effective date: 20211015 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602017046957 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG9D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20211229 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20211229 Ref country code: RS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MP Effective date: 20210929 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 1434249 Country of ref document: AT Kind code of ref document: T Effective date: 20210929 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20211230 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220129 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: RO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20220131 Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: NL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: ES Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: AL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602017046957 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20220630 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602017046957 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20220810 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220810 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220831 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220831 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MM Effective date: 20220831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220810 Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20230301 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20220810 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20170810 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: IT Payment date: 20250808 Year of fee payment: 9 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: FR Payment date: 20250828 Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20210929 |