EP2321197B1 - Package assembly for on-demand marination and method for providing the same - Google Patents
Package assembly for on-demand marination and method for providing the same Download PDFInfo
- Publication number
- EP2321197B1 EP2321197B1 EP20090791470 EP09791470A EP2321197B1 EP 2321197 B1 EP2321197 B1 EP 2321197B1 EP 20090791470 EP20090791470 EP 20090791470 EP 09791470 A EP09791470 A EP 09791470A EP 2321197 B1 EP2321197 B1 EP 2321197B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- package
- compartment
- seal
- food additive
- film
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Not-in-force
Links
- 238000000034 method Methods 0.000 title claims description 55
- 239000002778 food additive Substances 0.000 claims description 96
- 235000013373 food additive Nutrition 0.000 claims description 94
- 235000013305 food Nutrition 0.000 claims description 91
- 238000007789 sealing Methods 0.000 claims description 68
- 235000013372 meat Nutrition 0.000 claims description 41
- 239000002985 plastic film Substances 0.000 claims description 37
- 229920006255 plastic film Polymers 0.000 claims description 36
- 235000015090 marinades Nutrition 0.000 claims description 20
- 238000011068 loading method Methods 0.000 claims description 17
- 238000005192 partition Methods 0.000 claims description 15
- 238000003856 thermoforming Methods 0.000 claims description 14
- 239000012530 fluid Substances 0.000 claims description 10
- 238000004891 communication Methods 0.000 claims description 6
- 238000002156 mixing Methods 0.000 claims description 5
- 239000010410 layer Substances 0.000 description 77
- 102000035195 Peptidases Human genes 0.000 description 33
- 108091005804 Peptidases Proteins 0.000 description 33
- 239000004365 Protease Substances 0.000 description 30
- 229920001169 thermoplastic Polymers 0.000 description 21
- 229920001577 copolymer Polymers 0.000 description 20
- 239000000463 material Substances 0.000 description 20
- 235000019419 proteases Nutrition 0.000 description 20
- 238000004806 packaging method and process Methods 0.000 description 19
- 239000004416 thermosoftening plastic Substances 0.000 description 19
- VGGSQFUCUMXWEO-UHFFFAOYSA-N Ethene Chemical compound C=C VGGSQFUCUMXWEO-UHFFFAOYSA-N 0.000 description 18
- 239000005977 Ethylene Substances 0.000 description 18
- -1 polyethylene naphthalate Polymers 0.000 description 15
- 230000008569 process Effects 0.000 description 15
- 239000000853 adhesive Substances 0.000 description 14
- 230000001070 adhesive effect Effects 0.000 description 14
- 229920000642 polymer Polymers 0.000 description 14
- 239000007788 liquid Substances 0.000 description 13
- 239000000306 component Substances 0.000 description 11
- 230000004888 barrier function Effects 0.000 description 10
- 239000004711 α-olefin Substances 0.000 description 10
- 239000004952 Polyamide Substances 0.000 description 9
- 239000000796 flavoring agent Substances 0.000 description 9
- 229920002647 polyamide Polymers 0.000 description 9
- 229920000089 Cyclic olefin copolymer Polymers 0.000 description 8
- 239000005038 ethylene vinyl acetate Substances 0.000 description 8
- 239000000203 mixture Substances 0.000 description 8
- 150000008064 anhydrides Chemical class 0.000 description 7
- DQXBYHZEEUGOBF-UHFFFAOYSA-N but-3-enoic acid;ethene Chemical compound C=C.OC(=O)CC=C DQXBYHZEEUGOBF-UHFFFAOYSA-N 0.000 description 7
- 239000003795 chemical substances by application Substances 0.000 description 7
- 235000019634 flavors Nutrition 0.000 description 7
- 238000010438 heat treatment Methods 0.000 description 7
- 238000003475 lamination Methods 0.000 description 7
- 229920001200 poly(ethylene-vinyl acetate) Polymers 0.000 description 7
- 239000000047 product Substances 0.000 description 7
- 238000012546 transfer Methods 0.000 description 7
- 108010032088 Calpain Proteins 0.000 description 6
- 102000007590 Calpain Human genes 0.000 description 6
- 102000002704 Leucyl aminopeptidase Human genes 0.000 description 6
- 108010004098 Leucyl aminopeptidase Proteins 0.000 description 6
- 229920002292 Nylon 6 Polymers 0.000 description 6
- 229920000098 polyolefin Polymers 0.000 description 6
- 239000000565 sealant Substances 0.000 description 6
- 239000012815 thermoplastic material Substances 0.000 description 6
- 241000196324 Embryophyta Species 0.000 description 5
- 235000015278 beef Nutrition 0.000 description 5
- 238000001125 extrusion Methods 0.000 description 5
- 239000007789 gas Substances 0.000 description 5
- 239000012793 heat-sealing layer Substances 0.000 description 5
- 229920000554 ionomer Polymers 0.000 description 5
- 239000005033 polyvinylidene chloride Substances 0.000 description 5
- 229940024999 proteolytic enzymes for treatment of wounds and ulcers Drugs 0.000 description 5
- 235000013311 vegetables Nutrition 0.000 description 5
- 241000271566 Aves Species 0.000 description 4
- 241000194108 Bacillus licheniformis Species 0.000 description 4
- 241000194110 Bacillus sp. (in: Bacteria) Species 0.000 description 4
- 108010004032 Bromelains Proteins 0.000 description 4
- 241000283153 Cetacea Species 0.000 description 4
- 241000272201 Columbiformes Species 0.000 description 4
- 241000238557 Decapoda Species 0.000 description 4
- 241000287828 Gallus gallus Species 0.000 description 4
- 102000001398 Granzyme Human genes 0.000 description 4
- 108060005986 Granzyme Proteins 0.000 description 4
- 108010067372 Pancreatic elastase Proteins 0.000 description 4
- 102000016387 Pancreatic elastase Human genes 0.000 description 4
- 108090000526 Papain Proteins 0.000 description 4
- 229920001328 Polyvinylidene chloride Polymers 0.000 description 4
- 239000000654 additive Substances 0.000 description 4
- 235000019835 bromelain Nutrition 0.000 description 4
- 235000013330 chicken meat Nutrition 0.000 description 4
- 230000000295 complement effect Effects 0.000 description 4
- 238000003851 corona treatment Methods 0.000 description 4
- 229920000092 linear low density polyethylene Polymers 0.000 description 4
- 239000004707 linear low-density polyethylene Substances 0.000 description 4
- 229920001684 low density polyethylene Polymers 0.000 description 4
- 239000004702 low-density polyethylene Substances 0.000 description 4
- 235000019834 papain Nutrition 0.000 description 4
- 229940055729 papain Drugs 0.000 description 4
- 229920000728 polyester Polymers 0.000 description 4
- 239000004800 polyvinyl chloride Substances 0.000 description 4
- 229920000915 polyvinyl chloride Polymers 0.000 description 4
- 235000019833 protease Nutrition 0.000 description 4
- 230000005855 radiation Effects 0.000 description 4
- 239000000126 substance Substances 0.000 description 4
- 238000007666 vacuum forming Methods 0.000 description 4
- 241000251468 Actinopterygii Species 0.000 description 3
- 235000019687 Lamb Nutrition 0.000 description 3
- 239000004677 Nylon Substances 0.000 description 3
- 239000003963 antioxidant agent Substances 0.000 description 3
- 239000012298 atmosphere Substances 0.000 description 3
- 230000008901 benefit Effects 0.000 description 3
- 239000012267 brine Substances 0.000 description 3
- 238000007906 compression Methods 0.000 description 3
- 230000006835 compression Effects 0.000 description 3
- 238000012864 cross contamination Methods 0.000 description 3
- 208000028659 discharge Diseases 0.000 description 3
- 229920005648 ethylene methacrylic acid copolymer Polymers 0.000 description 3
- 238000007765 extrusion coating Methods 0.000 description 3
- 235000019688 fish Nutrition 0.000 description 3
- 238000007710 freezing Methods 0.000 description 3
- 230000008014 freezing Effects 0.000 description 3
- 238000005304 joining Methods 0.000 description 3
- 210000003205 muscle Anatomy 0.000 description 3
- 229920001778 nylon Polymers 0.000 description 3
- 229920003023 plastic Polymers 0.000 description 3
- 239000004033 plastic Substances 0.000 description 3
- 229920002959 polymer blend Polymers 0.000 description 3
- 244000144977 poultry Species 0.000 description 3
- 235000013594 poultry meat Nutrition 0.000 description 3
- 239000003755 preservative agent Substances 0.000 description 3
- HPALAKNZSZLMCH-UHFFFAOYSA-M sodium;chloride;hydrate Chemical compound O.[Na+].[Cl-] HPALAKNZSZLMCH-UHFFFAOYSA-M 0.000 description 3
- 235000013599 spices Nutrition 0.000 description 3
- 229920002397 thermoplastic olefin Polymers 0.000 description 3
- 210000001519 tissue Anatomy 0.000 description 3
- 238000011282 treatment Methods 0.000 description 3
- UUUHXMGGBIUAPW-UHFFFAOYSA-N 1-[1-[2-[[5-amino-2-[[1-[5-(diaminomethylideneamino)-2-[[1-[3-(1h-indol-3-yl)-2-[(5-oxopyrrolidine-2-carbonyl)amino]propanoyl]pyrrolidine-2-carbonyl]amino]pentanoyl]pyrrolidine-2-carbonyl]amino]-5-oxopentanoyl]amino]-3-methylpentanoyl]pyrrolidine-2-carbon Chemical compound C1CCC(C(=O)N2C(CCC2)C(O)=O)N1C(=O)C(C(C)CC)NC(=O)C(CCC(N)=O)NC(=O)C1CCCN1C(=O)C(CCCN=C(N)N)NC(=O)C1CCCN1C(=O)C(CC=1C2=CC=CC=C2NC=1)NC(=O)C1CCC(=O)N1 UUUHXMGGBIUAPW-UHFFFAOYSA-N 0.000 description 2
- CUVGUPIVTLGRGI-UHFFFAOYSA-N 4-(3-phosphonopropyl)piperazine-2-carboxylic acid Chemical compound OC(=O)C1CN(CCCP(O)(O)=O)CCN1 CUVGUPIVTLGRGI-UHFFFAOYSA-N 0.000 description 2
- LKDMKWNDBAVNQZ-UHFFFAOYSA-N 4-[[1-[[1-[2-[[1-(4-nitroanilino)-1-oxo-3-phenylpropan-2-yl]carbamoyl]pyrrolidin-1-yl]-1-oxopropan-2-yl]amino]-1-oxopropan-2-yl]amino]-4-oxobutanoic acid Chemical compound OC(=O)CCC(=O)NC(C)C(=O)NC(C)C(=O)N1CCCC1C(=O)NC(C(=O)NC=1C=CC(=CC=1)[N+]([O-])=O)CC1=CC=CC=C1 LKDMKWNDBAVNQZ-UHFFFAOYSA-N 0.000 description 2
- ODHCTXKNWHHXJC-VKHMYHEASA-N 5-oxo-L-proline Chemical compound OC(=O)[C@@H]1CCC(=O)N1 ODHCTXKNWHHXJC-VKHMYHEASA-N 0.000 description 2
- 235000001674 Agaricus brunnescens Nutrition 0.000 description 2
- 102000004400 Aminopeptidases Human genes 0.000 description 2
- 108090000915 Aminopeptidases Proteins 0.000 description 2
- 244000099147 Ananas comosus Species 0.000 description 2
- 235000007119 Ananas comosus Nutrition 0.000 description 2
- 241000272525 Anas platyrhynchos Species 0.000 description 2
- 108010001779 Ancrod Proteins 0.000 description 2
- 241000272814 Anser sp. Species 0.000 description 2
- 241000269350 Anura Species 0.000 description 2
- 241000228212 Aspergillus Species 0.000 description 2
- 240000006439 Aspergillus oryzae Species 0.000 description 2
- 235000002247 Aspergillus oryzae Nutrition 0.000 description 2
- 241000228251 Aspergillus phoenicis Species 0.000 description 2
- 241000131386 Aspergillus sojae Species 0.000 description 2
- 241000238017 Astacoidea Species 0.000 description 2
- 241000972773 Aulopiformes Species 0.000 description 2
- 241000237519 Bivalvia Species 0.000 description 2
- 241000282817 Bovidae Species 0.000 description 2
- 240000007124 Brassica oleracea Species 0.000 description 2
- 235000003899 Brassica oleracea var acephala Nutrition 0.000 description 2
- 235000011299 Brassica oleracea var botrytis Nutrition 0.000 description 2
- 235000012905 Brassica oleracea var viridis Nutrition 0.000 description 2
- 240000003259 Brassica oleracea var. botrytis Species 0.000 description 2
- 241000282836 Camelus dromedarius Species 0.000 description 2
- 241000283707 Capra Species 0.000 description 2
- 235000008534 Capsicum annuum var annuum Nutrition 0.000 description 2
- BVKZGUZCCUSVTD-UHFFFAOYSA-L Carbonate Chemical compound [O-]C([O-])=O BVKZGUZCCUSVTD-UHFFFAOYSA-L 0.000 description 2
- 108090000087 Carboxypeptidase B Proteins 0.000 description 2
- 102000003670 Carboxypeptidase B Human genes 0.000 description 2
- 108010006303 Carboxypeptidases Proteins 0.000 description 2
- 102000005367 Carboxypeptidases Human genes 0.000 description 2
- 108010080937 Carboxypeptidases A Proteins 0.000 description 2
- 102000000496 Carboxypeptidases A Human genes 0.000 description 2
- 235000009467 Carica papaya Nutrition 0.000 description 2
- 240000006432 Carica papaya Species 0.000 description 2
- 108090000397 Caspase 3 Proteins 0.000 description 2
- 102000004018 Caspase 6 Human genes 0.000 description 2
- 108090000425 Caspase 6 Proteins 0.000 description 2
- 108090000567 Caspase 7 Proteins 0.000 description 2
- 102100035904 Caspase-1 Human genes 0.000 description 2
- 108090000426 Caspase-1 Proteins 0.000 description 2
- 102000004068 Caspase-10 Human genes 0.000 description 2
- 108090000572 Caspase-10 Proteins 0.000 description 2
- 102000004066 Caspase-12 Human genes 0.000 description 2
- 108090000570 Caspase-12 Proteins 0.000 description 2
- 102000004046 Caspase-2 Human genes 0.000 description 2
- 108090000552 Caspase-2 Proteins 0.000 description 2
- 102100029855 Caspase-3 Human genes 0.000 description 2
- 102100025597 Caspase-4 Human genes 0.000 description 2
- 101710090338 Caspase-4 Proteins 0.000 description 2
- 102100038916 Caspase-5 Human genes 0.000 description 2
- 101710090333 Caspase-5 Proteins 0.000 description 2
- 102100038902 Caspase-7 Human genes 0.000 description 2
- 102000004091 Caspase-8 Human genes 0.000 description 2
- 108090000538 Caspase-8 Proteins 0.000 description 2
- 102000004039 Caspase-9 Human genes 0.000 description 2
- 108090000566 Caspase-9 Proteins 0.000 description 2
- 102000011727 Caspases Human genes 0.000 description 2
- 108010076667 Caspases Proteins 0.000 description 2
- 108010059081 Cathepsin A Proteins 0.000 description 2
- 102000005572 Cathepsin A Human genes 0.000 description 2
- 108090000712 Cathepsin B Proteins 0.000 description 2
- 102000004225 Cathepsin B Human genes 0.000 description 2
- 102000003902 Cathepsin C Human genes 0.000 description 2
- 108090000267 Cathepsin C Proteins 0.000 description 2
- 102000003908 Cathepsin D Human genes 0.000 description 2
- 108090000258 Cathepsin D Proteins 0.000 description 2
- 102000004173 Cathepsin G Human genes 0.000 description 2
- 108090000617 Cathepsin G Proteins 0.000 description 2
- 108090000619 Cathepsin H Proteins 0.000 description 2
- 102000004175 Cathepsin H Human genes 0.000 description 2
- 108090000624 Cathepsin L Proteins 0.000 description 2
- 102000004172 Cathepsin L Human genes 0.000 description 2
- 241000238366 Cephalopoda Species 0.000 description 2
- 241000282693 Cercopithecidae Species 0.000 description 2
- 241000282994 Cervidae Species 0.000 description 2
- 241000251730 Chondrichthyes Species 0.000 description 2
- 102100024539 Chymase Human genes 0.000 description 2
- 108090000227 Chymases Proteins 0.000 description 2
- 108090001069 Chymopapain Proteins 0.000 description 2
- 108090000746 Chymosin Proteins 0.000 description 2
- 108090000317 Chymotrypsin Proteins 0.000 description 2
- 241000252203 Clupea harengus Species 0.000 description 2
- 241000555825 Clupeidae Species 0.000 description 2
- 108060005980 Collagenase Proteins 0.000 description 2
- 102000029816 Collagenase Human genes 0.000 description 2
- 108090000044 Complement Factor I Proteins 0.000 description 2
- 102000003706 Complement factor D Human genes 0.000 description 2
- 108090000059 Complement factor D Proteins 0.000 description 2
- 102100035431 Complement factor I Human genes 0.000 description 2
- 241000938605 Crocodylia Species 0.000 description 2
- 241000270722 Crocodylidae Species 0.000 description 2
- 241000238424 Crustacea Species 0.000 description 2
- 102000016622 Dipeptidyl Peptidase 4 Human genes 0.000 description 2
- 108010067770 Endopeptidase K Proteins 0.000 description 2
- 108010013369 Enteropeptidase Proteins 0.000 description 2
- 102100029727 Enteropeptidase Human genes 0.000 description 2
- 229920000219 Ethylene vinyl alcohol Polymers 0.000 description 2
- 108010074860 Factor Xa Proteins 0.000 description 2
- 108010088842 Fibrinolysin Proteins 0.000 description 2
- 108090000270 Ficain Proteins 0.000 description 2
- 108090001126 Furin Proteins 0.000 description 2
- 102000004961 Furin Human genes 0.000 description 2
- 241000276438 Gadus morhua Species 0.000 description 2
- 101000930822 Giardia intestinalis Dipeptidyl-peptidase 4 Proteins 0.000 description 2
- 108010051815 Glutamyl endopeptidase Proteins 0.000 description 2
- 108010010369 HIV Protease Proteins 0.000 description 2
- 102000001399 Kallikrein Human genes 0.000 description 2
- 108060005987 Kallikrein Proteins 0.000 description 2
- FFEARJCKVFRZRR-BYPYZUCNSA-N L-methionine Chemical compound CSCC[C@H](N)C(O)=O FFEARJCKVFRZRR-BYPYZUCNSA-N 0.000 description 2
- 108010053229 Lysyl endopeptidase Proteins 0.000 description 2
- 241000289581 Macropus sp. Species 0.000 description 2
- 241000276489 Merlangius merlangus Species 0.000 description 2
- 102000005741 Metalloproteases Human genes 0.000 description 2
- 108010006035 Metalloproteases Proteins 0.000 description 2
- 101000933115 Mus musculus Caspase-4 Proteins 0.000 description 2
- 241000237536 Mytilus edulis Species 0.000 description 2
- 241000283973 Oryctolagus cuniculus Species 0.000 description 2
- 241000237502 Ostreidae Species 0.000 description 2
- 241000194105 Paenibacillus polymyxa Species 0.000 description 2
- 241001494479 Pecora Species 0.000 description 2
- 241000237503 Pectinidae Species 0.000 description 2
- 108090000284 Pepsin A Proteins 0.000 description 2
- 102000057297 Pepsin A Human genes 0.000 description 2
- 108090000882 Peptidyl-Dipeptidase A Proteins 0.000 description 2
- 102000004270 Peptidyl-Dipeptidase A Human genes 0.000 description 2
- 108010030544 Peptidyl-Lys metalloendopeptidase Proteins 0.000 description 2
- 235000010627 Phaseolus vulgaris Nutrition 0.000 description 2
- 244000046052 Phaseolus vulgaris Species 0.000 description 2
- 241000286209 Phasianidae Species 0.000 description 2
- 241000269907 Pleuronectes platessa Species 0.000 description 2
- 241000269980 Pleuronectidae Species 0.000 description 2
- 239000004793 Polystyrene Substances 0.000 description 2
- 108010059712 Pronase Proteins 0.000 description 2
- 108010072866 Prostate-Specific Antigen Proteins 0.000 description 2
- 102100038358 Prostate-specific antigen Human genes 0.000 description 2
- 101800004937 Protein C Proteins 0.000 description 2
- 101001091368 Rattus norvegicus Glandular kallikrein-7, submandibular/renal Proteins 0.000 description 2
- 241000157468 Reinhardtius hippoglossoides Species 0.000 description 2
- 108090000783 Renin Proteins 0.000 description 2
- 102100028255 Renin Human genes 0.000 description 2
- 241000952054 Rhizopus sp. Species 0.000 description 2
- 101000898773 Saccharomyces cerevisiae (strain ATCC 204508 / S288c) Saccharopepsin Proteins 0.000 description 2
- 241000277331 Salmonidae Species 0.000 description 2
- 101800001700 Saposin-D Proteins 0.000 description 2
- 102400000827 Saposin-D Human genes 0.000 description 2
- 241000270295 Serpentes Species 0.000 description 2
- FAPWRFPIFSIZLT-UHFFFAOYSA-M Sodium chloride Chemical compound [Na+].[Cl-] FAPWRFPIFSIZLT-UHFFFAOYSA-M 0.000 description 2
- 241000251778 Squalus acanthias Species 0.000 description 2
- 108010023197 Streptokinase Proteins 0.000 description 2
- 241000187392 Streptomyces griseus Species 0.000 description 2
- 108090000787 Subtilisin Proteins 0.000 description 2
- 108010056079 Subtilisins Proteins 0.000 description 2
- 102000005158 Subtilisins Human genes 0.000 description 2
- 241000282898 Sus scrofa Species 0.000 description 2
- 241000270666 Testudines Species 0.000 description 2
- 108090001109 Thermolysin Proteins 0.000 description 2
- 108090000190 Thrombin Proteins 0.000 description 2
- ISWQCIVKKSOKNN-UHFFFAOYSA-L Tiron Chemical compound [Na+].[Na+].OC1=CC(S([O-])(=O)=O)=CC(S([O-])(=O)=O)=C1O ISWQCIVKKSOKNN-UHFFFAOYSA-L 0.000 description 2
- 108090000373 Tissue Plasminogen Activator Proteins 0.000 description 2
- 102000003978 Tissue Plasminogen Activator Human genes 0.000 description 2
- 241000283907 Tragelaphus oryx Species 0.000 description 2
- 108090000631 Trypsin Proteins 0.000 description 2
- 102000004142 Trypsin Human genes 0.000 description 2
- 108060005989 Tryptase Proteins 0.000 description 2
- 102000001400 Tryptase Human genes 0.000 description 2
- 102000003990 Urokinase-type plasminogen activator Human genes 0.000 description 2
- 108090000435 Urokinase-type plasminogen activator Proteins 0.000 description 2
- 102100039662 Xaa-Pro dipeptidase Human genes 0.000 description 2
- 241000269959 Xiphias gladius Species 0.000 description 2
- 229960004233 ancrod Drugs 0.000 description 2
- 230000000844 anti-bacterial effect Effects 0.000 description 2
- QVGXLLKOCUKJST-UHFFFAOYSA-N atomic oxygen Chemical compound [O] QVGXLLKOCUKJST-UHFFFAOYSA-N 0.000 description 2
- 239000003899 bactericide agent Substances 0.000 description 2
- 239000011324 bead Substances 0.000 description 2
- 108010054847 carboxypeptidase P Proteins 0.000 description 2
- 108010018550 caspase 13 Proteins 0.000 description 2
- 229960002976 chymopapain Drugs 0.000 description 2
- 229960002376 chymotrypsin Drugs 0.000 description 2
- 235000020639 clam Nutrition 0.000 description 2
- 108090001092 clostripain Proteins 0.000 description 2
- 229960002424 collagenase Drugs 0.000 description 2
- 238000010411 cooking Methods 0.000 description 2
- 238000002788 crimping Methods 0.000 description 2
- 238000004132 cross linking Methods 0.000 description 2
- 108090000200 cucumisin Proteins 0.000 description 2
- 210000000172 cytosol Anatomy 0.000 description 2
- 239000006185 dispersion Substances 0.000 description 2
- 238000009826 distribution Methods 0.000 description 2
- 239000000975 dye Substances 0.000 description 2
- 108010003914 endoproteinase Asp-N Proteins 0.000 description 2
- 125000000816 ethylene group Chemical group [H]C([H])([*:1])C([H])([H])[*:2] 0.000 description 2
- 239000004715 ethylene vinyl alcohol Substances 0.000 description 2
- 235000019836 ficin Nutrition 0.000 description 2
- POTUGHMKJGOKRI-UHFFFAOYSA-N ficin Chemical compound FI=CI=N POTUGHMKJGOKRI-UHFFFAOYSA-N 0.000 description 2
- 235000013355 food flavoring agent Nutrition 0.000 description 2
- 239000000417 fungicide Substances 0.000 description 2
- 108010062699 gamma-Glutamyl Hydrolase Proteins 0.000 description 2
- 235000008216 herbs Nutrition 0.000 description 2
- 235000019514 herring Nutrition 0.000 description 2
- 239000004615 ingredient Substances 0.000 description 2
- 230000000977 initiatory effect Effects 0.000 description 2
- 210000000265 leukocyte Anatomy 0.000 description 2
- 241000238565 lobster Species 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 239000011159 matrix material Substances 0.000 description 2
- 235000013622 meat product Nutrition 0.000 description 2
- 238000002844 melting Methods 0.000 description 2
- 108010003855 mesentericopeptidase Proteins 0.000 description 2
- 229930182817 methionine Natural products 0.000 description 2
- 108010009355 microbial metalloproteinases Proteins 0.000 description 2
- 230000003228 microsomal effect Effects 0.000 description 2
- 235000020638 mussel Nutrition 0.000 description 2
- 229920006113 non-polar polymer Polymers 0.000 description 2
- 239000001301 oxygen Substances 0.000 description 2
- 229910052760 oxygen Inorganic materials 0.000 description 2
- 235000020636 oyster Nutrition 0.000 description 2
- 239000012785 packaging film Substances 0.000 description 2
- 229920006280 packaging film Polymers 0.000 description 2
- 238000000059 patterning Methods 0.000 description 2
- 229940111202 pepsin Drugs 0.000 description 2
- 229940012957 plasmin Drugs 0.000 description 2
- 229920006112 polar polymer Polymers 0.000 description 2
- 229920003207 poly(ethylene-2,6-naphthalate) Polymers 0.000 description 2
- 229920002239 polyacrylonitrile Polymers 0.000 description 2
- 229920001281 polyalkylene Polymers 0.000 description 2
- 229920001748 polybutylene Polymers 0.000 description 2
- 239000011112 polyethylene naphthalate Substances 0.000 description 2
- 229920002223 polystyrene Polymers 0.000 description 2
- 239000000843 powder Substances 0.000 description 2
- 108010066823 proline dipeptidase Proteins 0.000 description 2
- 229920001384 propylene homopolymer Polymers 0.000 description 2
- 108010043535 protease S Proteins 0.000 description 2
- 229960000856 protein c Drugs 0.000 description 2
- 102000004169 proteins and genes Human genes 0.000 description 2
- 108090000623 proteins and genes Proteins 0.000 description 2
- 238000004080 punching Methods 0.000 description 2
- 229940043131 pyroglutamate Drugs 0.000 description 2
- 230000009467 reduction Effects 0.000 description 2
- 229920005989 resin Polymers 0.000 description 2
- 239000011347 resin Substances 0.000 description 2
- 235000019515 salmon Nutrition 0.000 description 2
- 235000019512 sardine Nutrition 0.000 description 2
- 235000020637 scallop Nutrition 0.000 description 2
- 238000009958 sewing Methods 0.000 description 2
- 235000015170 shellfish Nutrition 0.000 description 2
- 239000000243 solution Substances 0.000 description 2
- 229960005202 streptokinase Drugs 0.000 description 2
- 108010059339 submandibular proteinase A Proteins 0.000 description 2
- 235000021335 sword fish Nutrition 0.000 description 2
- 229960004072 thrombin Drugs 0.000 description 2
- 229960000187 tissue plasminogen activator Drugs 0.000 description 2
- 239000012588 trypsin Substances 0.000 description 2
- 229960001322 trypsin Drugs 0.000 description 2
- 229960005356 urokinase Drugs 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- 239000000080 wetting agent Substances 0.000 description 2
- 238000003855 Adhesive Lamination Methods 0.000 description 1
- 235000005254 Allium ampeloprasum Nutrition 0.000 description 1
- 240000006108 Allium ampeloprasum Species 0.000 description 1
- 244000291564 Allium cepa Species 0.000 description 1
- 235000002732 Allium cepa var. cepa Nutrition 0.000 description 1
- 240000007087 Apium graveolens Species 0.000 description 1
- 235000015849 Apium graveolens Dulce Group Nutrition 0.000 description 1
- 235000010591 Appio Nutrition 0.000 description 1
- 235000017060 Arachis glabrata Nutrition 0.000 description 1
- 244000105624 Arachis hypogaea Species 0.000 description 1
- 235000010777 Arachis hypogaea Nutrition 0.000 description 1
- 235000018262 Arachis monticola Nutrition 0.000 description 1
- 244000003416 Asparagus officinalis Species 0.000 description 1
- 235000005340 Asparagus officinalis Nutrition 0.000 description 1
- 235000016068 Berberis vulgaris Nutrition 0.000 description 1
- 241000335053 Beta vulgaris Species 0.000 description 1
- 235000011332 Brassica juncea Nutrition 0.000 description 1
- 244000178993 Brassica juncea Species 0.000 description 1
- 235000011293 Brassica napus Nutrition 0.000 description 1
- 240000002791 Brassica napus Species 0.000 description 1
- 235000011301 Brassica oleracea var capitata Nutrition 0.000 description 1
- 235000017647 Brassica oleracea var italica Nutrition 0.000 description 1
- 235000001169 Brassica oleracea var oleracea Nutrition 0.000 description 1
- 240000004073 Brassica oleracea var. viridis Species 0.000 description 1
- 235000000540 Brassica rapa subsp rapa Nutrition 0.000 description 1
- 235000002566 Capsicum Nutrition 0.000 description 1
- 240000004160 Capsicum annuum Species 0.000 description 1
- 240000008384 Capsicum annuum var. annuum Species 0.000 description 1
- 235000007862 Capsicum baccatum Nutrition 0.000 description 1
- 235000005979 Citrus limon Nutrition 0.000 description 1
- 244000131522 Citrus pyriformis Species 0.000 description 1
- 235000009854 Cucurbita moschata Nutrition 0.000 description 1
- 240000001980 Cucurbita pepo Species 0.000 description 1
- 235000009852 Cucurbita pepo Nutrition 0.000 description 1
- 241000219130 Cucurbita pepo subsp. pepo Species 0.000 description 1
- 235000003954 Cucurbita pepo var melopepo Nutrition 0.000 description 1
- 244000019459 Cynara cardunculus Species 0.000 description 1
- 235000019106 Cynara scolymus Nutrition 0.000 description 1
- 235000002767 Daucus carota Nutrition 0.000 description 1
- 244000000626 Daucus carota Species 0.000 description 1
- 108010082495 Dietary Plant Proteins Proteins 0.000 description 1
- 229920003939 DuPont™ Surlyn® 1650 Polymers 0.000 description 1
- 244000133098 Echinacea angustifolia Species 0.000 description 1
- 229920003345 Elvax® Polymers 0.000 description 1
- 102000004190 Enzymes Human genes 0.000 description 1
- 108090000790 Enzymes Proteins 0.000 description 1
- WQZGKKKJIJFFOK-GASJEMHNSA-N Glucose Natural products OC[C@H]1OC(O)[C@H](O)[C@@H](O)[C@@H]1O WQZGKKKJIJFFOK-GASJEMHNSA-N 0.000 description 1
- 235000010469 Glycine max Nutrition 0.000 description 1
- VEXZGXHMUGYJMC-UHFFFAOYSA-N Hydrochloric acid Chemical compound Cl VEXZGXHMUGYJMC-UHFFFAOYSA-N 0.000 description 1
- 235000017309 Hypericum perforatum Nutrition 0.000 description 1
- 244000141009 Hypericum perforatum Species 0.000 description 1
- DGAQECJNVWCQMB-PUAWFVPOSA-M Ilexoside XXIX Chemical compound C[C@@H]1CC[C@@]2(CC[C@@]3(C(=CC[C@H]4[C@]3(CC[C@@H]5[C@@]4(CC[C@@H](C5(C)C)OS(=O)(=O)[O-])C)C)[C@@H]2[C@]1(C)O)C)C(=O)O[C@H]6[C@@H]([C@H]([C@@H]([C@H](O6)CO)O)O)O.[Na+] DGAQECJNVWCQMB-PUAWFVPOSA-M 0.000 description 1
- 235000002678 Ipomoea batatas Nutrition 0.000 description 1
- 244000017020 Ipomoea batatas Species 0.000 description 1
- 235000005135 Micromeria juliana Nutrition 0.000 description 1
- 235000017879 Nasturtium officinale Nutrition 0.000 description 1
- 240000005407 Nasturtium officinale Species 0.000 description 1
- 239000006057 Non-nutritive feed additive Substances 0.000 description 1
- 240000007594 Oryza sativa Species 0.000 description 1
- 235000007164 Oryza sativa Nutrition 0.000 description 1
- 229910019142 PO4 Inorganic materials 0.000 description 1
- 235000003283 Pachira macrocarpa Nutrition 0.000 description 1
- 241000758706 Piperaceae Species 0.000 description 1
- 235000010582 Pisum sativum Nutrition 0.000 description 1
- 240000004713 Pisum sativum Species 0.000 description 1
- 229920000034 Plastomer Polymers 0.000 description 1
- 239000004698 Polyethylene Substances 0.000 description 1
- 239000004743 Polypropylene Substances 0.000 description 1
- 244000088415 Raphanus sativus Species 0.000 description 1
- 235000006140 Raphanus sativus var sativus Nutrition 0.000 description 1
- 244000299790 Rheum rhabarbarum Species 0.000 description 1
- 235000009411 Rheum rhabarbarum Nutrition 0.000 description 1
- 235000007315 Satureja hortensis Nutrition 0.000 description 1
- 240000002114 Satureja hortensis Species 0.000 description 1
- 235000002597 Solanum melongena Nutrition 0.000 description 1
- 244000061458 Solanum melongena Species 0.000 description 1
- 235000002595 Solanum tuberosum Nutrition 0.000 description 1
- 244000061456 Solanum tuberosum Species 0.000 description 1
- 235000009337 Spinacia oleracea Nutrition 0.000 description 1
- 244000300264 Spinacia oleracea Species 0.000 description 1
- 229920002472 Starch Polymers 0.000 description 1
- 235000014364 Trapa natans Nutrition 0.000 description 1
- 240000001085 Trapa natans Species 0.000 description 1
- 240000008042 Zea mays Species 0.000 description 1
- 235000005824 Zea mays ssp. parviglumis Nutrition 0.000 description 1
- 235000002017 Zea mays subsp mays Nutrition 0.000 description 1
- HCHKCACWOHOZIP-UHFFFAOYSA-N Zinc Chemical compound [Zn] HCHKCACWOHOZIP-UHFFFAOYSA-N 0.000 description 1
- 238000005299 abrasion Methods 0.000 description 1
- 238000010521 absorption reaction Methods 0.000 description 1
- 239000002253 acid Substances 0.000 description 1
- 230000002378 acidificating effect Effects 0.000 description 1
- 239000005030 aluminium foil Substances 0.000 description 1
- 239000004599 antimicrobial Substances 0.000 description 1
- 230000003078 antioxidant effect Effects 0.000 description 1
- 239000002216 antistatic agent Substances 0.000 description 1
- 235000016520 artichoke thistle Nutrition 0.000 description 1
- 235000013527 bean curd Nutrition 0.000 description 1
- 230000005250 beta ray Effects 0.000 description 1
- WQZGKKKJIJFFOK-VFUOTHLCSA-N beta-D-glucose Chemical compound OC[C@H]1O[C@@H](O)[C@H](O)[C@@H](O)[C@@H]1O WQZGKKKJIJFFOK-VFUOTHLCSA-N 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 229920000891 common polymer Polymers 0.000 description 1
- 239000012141 concentrate Substances 0.000 description 1
- 235000008504 concentrate Nutrition 0.000 description 1
- 238000009833 condensation Methods 0.000 description 1
- 230000005494 condensation Effects 0.000 description 1
- 238000011109 contamination Methods 0.000 description 1
- 238000001816 cooling Methods 0.000 description 1
- 235000005822 corn Nutrition 0.000 description 1
- 239000013078 crystal Substances 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 230000032798 delamination Effects 0.000 description 1
- 230000001419 dependent effect Effects 0.000 description 1
- 239000008121 dextrose Substances 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 235000014134 echinacea Nutrition 0.000 description 1
- 235000013399 edible fruits Nutrition 0.000 description 1
- 229920001971 elastomer Polymers 0.000 description 1
- 239000000806 elastomer Substances 0.000 description 1
- 230000002255 enzymatic effect Effects 0.000 description 1
- 229940088598 enzyme Drugs 0.000 description 1
- 229940026231 erythorbate Drugs 0.000 description 1
- 235000010350 erythorbic acid Nutrition 0.000 description 1
- UFRKOOWSQGXVKV-UHFFFAOYSA-N ethene;ethenol Chemical compound C=C.OC=C UFRKOOWSQGXVKV-UHFFFAOYSA-N 0.000 description 1
- 239000010685 fatty oil Substances 0.000 description 1
- 239000000945 filler Substances 0.000 description 1
- 238000011049 filling Methods 0.000 description 1
- 235000013312 flour Nutrition 0.000 description 1
- 230000009969 flowable effect Effects 0.000 description 1
- 235000012041 food component Nutrition 0.000 description 1
- 239000005428 food component Substances 0.000 description 1
- 238000009472 formulation Methods 0.000 description 1
- 235000013611 frozen food Nutrition 0.000 description 1
- 235000011389 fruit/vegetable juice Nutrition 0.000 description 1
- 230000000855 fungicidal effect Effects 0.000 description 1
- 230000004927 fusion Effects 0.000 description 1
- 230000005251 gamma ray Effects 0.000 description 1
- RZXDTJIXPSCHCI-UHFFFAOYSA-N hexa-1,5-diene-2,5-diol Chemical compound OC(=C)CCC(O)=C RZXDTJIXPSCHCI-UHFFFAOYSA-N 0.000 description 1
- 229920001519 homopolymer Polymers 0.000 description 1
- 238000002347 injection Methods 0.000 description 1
- 239000007924 injection Substances 0.000 description 1
- 229910052500 inorganic mineral Inorganic materials 0.000 description 1
- 235000021374 legumes Nutrition 0.000 description 1
- 235000021056 liquid food Nutrition 0.000 description 1
- 239000011344 liquid material Substances 0.000 description 1
- 244000144972 livestock Species 0.000 description 1
- 230000001050 lubricating effect Effects 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 230000000813 microbial effect Effects 0.000 description 1
- 239000011707 mineral Substances 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 239000003607 modifier Substances 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
- 150000002826 nitrites Chemical class 0.000 description 1
- 239000003921 oil Substances 0.000 description 1
- 235000019198 oils Nutrition 0.000 description 1
- 230000003647 oxidation Effects 0.000 description 1
- 238000007254 oxidation reaction Methods 0.000 description 1
- 239000005022 packaging material Substances 0.000 description 1
- 235000021485 packed food Nutrition 0.000 description 1
- 239000006072 paste Substances 0.000 description 1
- 235000020232 peanut Nutrition 0.000 description 1
- 235000021317 phosphate Nutrition 0.000 description 1
- 150000003013 phosphoric acid derivatives Chemical class 0.000 description 1
- 239000000049 pigment Substances 0.000 description 1
- 229920000573 polyethylene Polymers 0.000 description 1
- 229920005638 polyethylene monopolymer Polymers 0.000 description 1
- 238000006116 polymerization reaction Methods 0.000 description 1
- 229920001155 polypropylene Polymers 0.000 description 1
- 229920000136 polysorbate Polymers 0.000 description 1
- 239000011527 polyurethane coating Substances 0.000 description 1
- 235000015277 pork Nutrition 0.000 description 1
- 235000012015 potatoes Nutrition 0.000 description 1
- 230000002028 premature Effects 0.000 description 1
- 230000002335 preservative effect Effects 0.000 description 1
- 238000003825 pressing Methods 0.000 description 1
- 238000012545 processing Methods 0.000 description 1
- 230000002035 prolonged effect Effects 0.000 description 1
- 239000002516 radical scavenger Substances 0.000 description 1
- 230000004044 response Effects 0.000 description 1
- 238000012552 review Methods 0.000 description 1
- 235000009566 rice Nutrition 0.000 description 1
- 235000009165 saligot Nutrition 0.000 description 1
- 150000003839 salts Chemical class 0.000 description 1
- 235000015067 sauces Nutrition 0.000 description 1
- 235000013580 sausages Nutrition 0.000 description 1
- 235000014102 seafood Nutrition 0.000 description 1
- 230000001953 sensory effect Effects 0.000 description 1
- 238000007493 shaping process Methods 0.000 description 1
- 239000002356 single layer Substances 0.000 description 1
- 239000012748 slip agent Substances 0.000 description 1
- 239000000779 smoke Substances 0.000 description 1
- 239000011734 sodium Substances 0.000 description 1
- 229910052708 sodium Inorganic materials 0.000 description 1
- 239000011780 sodium chloride Substances 0.000 description 1
- 239000011343 solid material Substances 0.000 description 1
- 239000012265 solid product Substances 0.000 description 1
- 235000013555 soy sauce Nutrition 0.000 description 1
- 239000003549 soybean oil Substances 0.000 description 1
- 235000012424 soybean oil Nutrition 0.000 description 1
- 235000020354 squash Nutrition 0.000 description 1
- 239000003381 stabilizer Substances 0.000 description 1
- 235000019698 starch Nutrition 0.000 description 1
- 235000000346 sugar Nutrition 0.000 description 1
- 150000008163 sugars Chemical class 0.000 description 1
- 230000003746 surface roughness Effects 0.000 description 1
- 239000000454 talc Substances 0.000 description 1
- 229910052623 talc Inorganic materials 0.000 description 1
- 235000013548 tempeh Nutrition 0.000 description 1
- 229920001897 terpolymer Polymers 0.000 description 1
- 238000012360 testing method Methods 0.000 description 1
- 238000010257 thawing Methods 0.000 description 1
- 239000003017 thermal stabilizer Substances 0.000 description 1
- 229920006345 thermoplastic polyamide Polymers 0.000 description 1
- 210000003813 thumb Anatomy 0.000 description 1
- 235000021419 vinegar Nutrition 0.000 description 1
- 239000000052 vinegar Substances 0.000 description 1
- 230000000007 visual effect Effects 0.000 description 1
- 239000011782 vitamin Substances 0.000 description 1
- 229940088594 vitamin Drugs 0.000 description 1
- 229930003231 vitamin Natural products 0.000 description 1
- 235000013343 vitamin Nutrition 0.000 description 1
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 1
- 239000011701 zinc Substances 0.000 description 1
- 229910052725 zinc Inorganic materials 0.000 description 1
Images




Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D81/00—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents
- B65D81/32—Containers, packaging elements, or packages, for contents presenting particular transport or storage problems, or adapted to be used for non-packaging purposes after removal of contents for packaging two or more different materials which must be maintained separate prior to use in admixture
- B65D81/3294—Thermoformed trays or the like with a plurality of recesses for different materials located in different recesses
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B65—CONVEYING; PACKING; STORING; HANDLING THIN OR FILAMENTARY MATERIAL
- B65D—CONTAINERS FOR STORAGE OR TRANSPORT OF ARTICLES OR MATERIALS, e.g. BAGS, BARRELS, BOTTLES, BOXES, CANS, CARTONS, CRATES, DRUMS, JARS, TANKS, HOPPERS, FORWARDING CONTAINERS; ACCESSORIES, CLOSURES, OR FITTINGS THEREFOR; PACKAGING ELEMENTS; PACKAGES
- B65D77/00—Packages formed by enclosing articles or materials in preformed containers, e.g. boxes, cartons, sacks or bags
- B65D77/04—Articles or materials enclosed in two or more containers disposed one within another
- B65D77/0446—Articles or materials enclosed in two or more containers disposed one within another the inner and outer containers being rigid or semi-rigid and the outer container being of polygonal cross-section not formed by folding or erecting one or more blanks
- B65D77/0453—Articles or materials enclosed in two or more containers disposed one within another the inner and outer containers being rigid or semi-rigid and the outer container being of polygonal cross-section not formed by folding or erecting one or more blanks the inner container having a polygonal cross-section
- B65D77/046—Articles or materials enclosed in two or more containers disposed one within another the inner and outer containers being rigid or semi-rigid and the outer container being of polygonal cross-section not formed by folding or erecting one or more blanks the inner container having a polygonal cross-section and being a tray or like shallow container
-
- A—HUMAN NECESSITIES
- A23—FOODS OR FOODSTUFFS; TREATMENT THEREOF, NOT COVERED BY OTHER CLASSES
- A23L—FOODS, FOODSTUFFS OR NON-ALCOHOLIC BEVERAGES, NOT OTHERWISE PROVIDED FOR; PREPARATION OR TREATMENT THEREOF
- A23L29/00—Foods or foodstuffs containing additives; Preparation or treatment thereof
Definitions
- tenderness is perhaps the trait most highly desired by consumers. Consequently, meat tenderness is a factor of major economic importance to the livestock and meat industries. Accordingly, the consumer acceptance of meat, e.g., beef, pork and poultry, depends to a large measure on the tenderness of the meat after cooking. When the meat is tough and fibrous, consumer acceptance is quite low. Meat prepared for home consumption and sold in local groceries and butcheries is normally of the more tender grades. For example, in the case of beef, lot feeding can be required to develop the desired amount of tenderness in the muscle tissue, including increases in fat content. However, such efforts can considerably increase the cost of the meat. For this reason, significant effort has been expended in the art to provide methods for tenderizing less tender grades of meat.
- food additives can be used to enhance the qualities of meats by providing enhanced visual appearance and tenderness from spices and flavorings.
- some techniques utilize injection of flavorings into the muscle to impart flavor and juiciness prior to packaging the meat.
- Other techniques include a means of tumbling a meat product in a marinade prior to packaging.
- the use of a tenderizer is often omitted because the proteolytic enzyme associated with tenderizing agents can overly soften the meat, resulting in an unsatisfactory texture.
- the over-tenderizing results from prolonged contact time between the meat and the tenderizing agent as a consequence of the poor ability to control the exposure time during distribution.
- the quality of a pre-marinated package is necessarily inconsistent as the meat generally is exposed for too long to the flavorants.
- restaurants or consumers can purchase a vacuum packaged meat package, cut open the package, and transfer the meat to a second bag wherein a marinade is added, or to a tray or vat that is loaded with a marinade.
- a marinade is added
- a tray or vat that is loaded with a marinade.
- a consumer removes the meat from its shipment package and necessarily exposes the meat to outside conditions that can introduce contamination during marinating.
- the method can introduce the undesirable step of cleaning the tray or vat to prevent cross-contamination.
- a multi-chamber package comprising a base that forms a pair of wells separated by a rib, a first component may be placed in the well, while a second component can be placed in the well.
- a first film which may be transparent and gas permeable, extends across the entirety of both wells and has a strong seal at the periphery of the package.
- a weaker seal is defined in the area of the rib between the two wells.
- a second film which may be gas impermeable aluminium foil, extends across the opening of the well. When a user presses on the second film, the weaker seal releases such that the components mix.
- the transparency of the first film may allow the user to know when the components are fully mixed and ready for use.
- FR 2 642 726 discloses a separate container for storing a first food item in a first compartment of a tray that cannot then be admixed with a second food item in a second compartment of the tray prior to opening the complete package assembly.
- the presently disclosed subject matter provides, among other things, a package assembly that includes first and second packages that maintains two or more components, e.g., a food additive and a food product, separately until a user desires to mix the two components within the package assembly.
- first and second packages that maintains two or more components, e.g., a food additive and a food product, separately until a user desires to mix the two components within the package assembly.
- the present invention provides a package assembly as defined in claim 1 essentially, comprising: a first package comprising a first compartment that substantially contains a second package and a second compartment configured to contain a food product; and the second package is configured to contain a food additive and includes a rupturable seal configured to rupture and allow the food additive to escape the second package when exposed to a predetermined pressure, wherein the second package is in fluid communication with the second compartment upon a rupturing of the rupturable seal so as to allow the food additive to mix with the food product, and wherein the first package is configured to withstand the predetermined pressure and prevent leaking of the food additive and food product from the first package during the mixing of the food additive and the food product.
- the present invention also provides a method of forming such a package assembly for controlling a level of food additive imparted to a food product as defined in claim 10, the method essentially comprising: forming a support member of a first package that includes a first compartment configured substantially to contain a second package and a second compartment configured to contain a food product; forming the second package configured to contain a food additive; loading the food additive into the second package; sealing the food additive in the second package with at least a rupturable seal configured to rupture and allow the food additive to escape the second package; loading the food product into the second compartment of the first package; loading the second package substantially into the first compartment of the first package such that the second package is in fluid communication with the second compartment of the first package upon a rupturing of the rupturable seal so as to allow the food additive to mix with the food product; and sealing the support member of the first package with a cover of the first package such that the first package is configured to withstand the predetermined pressure and prevent leaking of the food additive and food product from the first package during the
- a package assembly for marinating a food product is provided.
- the first package may include a first plastic film and a second plastic film and the hard seal of the first package may extend around the perimeter of the first plastic film and the perimeter of the second plastic film.
- the first plastic film may be a thermoformed film formed into a compartmented support member having the first and second compartments.
- the second package may include a first plastic film and a second plastic film.
- the first plastic film may be a thermoformed film formed into a compartmented support member having a compartment.
- the first plastic film of the second package and the second plastic film of the second package may collectively form a flange of the second package extending away from the compartment and the rupturable seal may extend at least across the flange of the second package.
- the rupturable seal may extend around the perimeters of the first and second plastic films of the second package including across the flange.
- the first and second compartments of the first package may be separated by a partition and the flange of the second package may extend from the compartment of the second package at least partially across the partition toward the second compartment of the fist package.
- the package assembly may further include a seal between the flange and the first plastic film of the first package and a seal between the flange and the second plastic film of the first package.
- the food additive may be selected from the group comprising: marinade, proteolytic enzyme, bactericide, fungicide, preservative, wetting agent, antioxidant, viscosity control agent, brine, curing agent, flavoring agent, and combinations thereof.
- the food product may be selected from the group comprising: meat, vegetable, and combinations thereof.
- the forming of the supporting member according to method claim 10 may include thermoforming a first plastic film of the first package.
- the forming of the second packaging may include thermoforming a first plastic film of the second package into a support member of the second package having a compartment of the second package.
- the loading the second package substantially into the first compartment of the first package may include positioning a flange of the second package at least partially across a partition separating the first compartment of the first package and the second compartment of the first package such that the flange extends from the first compartment of the first package toward the second compartment of the second package.
- a package e.g., "a marinade package”
- a marinade package includes a plurality of such packages, and so forth.
- the term "about”, when referring to a value or to an amount of mass, weight, time, volume, concentration, percentage, and the like can encompass variations of, in some embodiments ⁇ 20%, in some embodiments ⁇ 10%, in some embodiments ⁇ 5%, in some embodiments ⁇ 1%, in some embodiments ⁇ 0.5%, and in some embodiments ⁇ 0.1%, from the specified amount, as such variations are appropriate in the disclosed package and methods.
- an abuse layer refers to an outer film layer and/or an inner film layer, so long as the film layer serves to resist abrasion, puncture, and other potential causes of reduction of package integrity, as well as potential causes of reduction of package appearance quality.
- Abuse layers can comprise any polymer, so long as the polymer contributes to achieving an integrity goal and/or an appearance goal.
- an abuse layer can comprise polymers having a modulus of at least 10 7 Pascals, at room temperature.
- an abuse layer can comprise, but is not limited to, polyamide and/or ethylene/propylene copolymer; in some embodiments, nylon 6, nylon 6/6, and/or amorphous nylon.
- the term "barrier”, and the phrase “barrier layer”, as applied to films and/or layers, can be used with reference to the ability of a film or layer to serve as a barrier to one or more gases.
- oxygen (i.e., gaseous 0 2 ) barrier layers have included, for example, ethylene/vinyl alcohol copolymer (polymerized ethylene vinyl alcohol), polyvinyl chloride, polyvinylidene chloride (PVDC), polyalkylene carbonate, polyamide, polyethylene naphthalate, polyester, polyacrylonitrile, and the like, as known to those of ordinary skill in the art.
- the 0 2 -barrier layer can comprise ethylene/vinyl alcohol copolymer, polyvinyl chloride, polyvinylidene chloride, and/or polyamide.
- corona treatment and “corona discharge treatment” refer to subjecting the surfaces of thermoplastic materials, such as polyolefins, to corona discharge, i.e., the ionization of a gas such as air in close proximity to a film surface, the ionization initiated by a high voltage passed through a nearby electrode, and causing oxidation and other changes to the film surface, such as surface roughness.
- Corona treatment of polymeric materials is disclosed in U.S. Patent No. 4,120,716, to Bonet .
- U.S. Patent No. 4,879,43 to Hoffman discloses the use of corona discharge for the treatment of plastic webs for use in meat cook-in packaging, with the corona treatment of the inside surface of the web to increase the adhesion of the meat to the proteinaceous material.
- film can be used in a generic sense to include plastic web, regardless of whether it is film or sheet.
- the term "food additive” refers to any liquid or solid material that results or can reasonably be expected to result, directly or indirectly, in its becoming a component or otherwise affecting the characteristics of any food product.
- the food additive can, for example, be an agent having a distinct taste and/or flavor, such as a salt or any other taste or flavor potentiator or modifier.
- examples of food additives include, but are not limited to, marinades and proteolytic enzymes.
- components that by themselves are not additives, such as vitamins, minerals, color additives, herbal additives (e.g., echinacea or St. John's Wort), antimicrobials, preservatives, and the like can be considered food additives.
- food product refers to any nourishing substance that is eaten or otherwise taken into the body to sustain life, provide energy, promote growth, and/or the like.
- food products can include, but are not limited to, meats, vegetables, fruits, starches, and combinations thereof.
- food products can include individual food components or mixtures thereof.
- heat seal refers to any seal of a first region of a film surface to a second region of a film surface, wherein the seal is formed by heating the regions to at least their respective seal initiation temperatures.
- Heat-sealing is the process of joining two or more thermoplastic films or sheets by heating areas in contact with each other to the temperature at which fusion occurs, usually aided by pressure.
- heat-sealing can be inclusive of thermal sealing, melt-bead sealing, impulse sealing, dielectric sealing, and/or ultrasonic sealing.
- the heating can be performed by any one or more of a wide variety of means, such as (but not limited to) a heated bar, hot wire, hot air, infrared radiation, ultrasonic sealing, and the like.
- lamination can refer to the process and resulting product made by bonding together two or more layers of film and/or other materials. Lamination can be accomplished by joining film layers with adhesives, joining with heat and pressure, spread coating, and/or extrusion coating.
- laminate can be inclusive of coextruded multilayer films comprising one or more tie layers.
- the term "marinade” refers to an edible substance that can impart one or more flavors and/or textures to a food product.
- the marinade can comprise acidic ingredients, such as vinegar, lemon juice, and/or wine.
- the marinade can comprise savory ingredients, such as soy sauce, brine, or other prepared sauces.
- the marinade can comprise oils, herbs, and spices to further flavor a food item.
- the marinade can comprise one or more proteolytic enzymes to flavor the food and/or to tenderize a food product.
- the term "meat” comprises both cooked and uncooked meat and includes, but is not limited to, beef, birds such as poultry (including chicken, duck, goose, turkey, and the like), buffalo, camel, crustacean (including shellfish, clams, scallops, mussels, oysters, lobster, crayfish, crab, shrimp, prawns, and the like), dog, fish (including salmon, trout, eel, cod, herring, plaice, whiting, halibut, turbot, ling, squid, tuna, sardines, swordfish, dogfish, shark, and the like), game (including deer, eland, antelope, and the like), game birds (such as pigeon, quail, doves, and the like), goat, hare, horse, kangaroo, lamb, marine mammals (including whales and the like), amphibians (including frogs and the like), monkey, pig, rabbit, reptiles (including turtles, snakes,
- the term "oriented” refers to a polymer-containing material that has been stretched at an elevated temperature (the orientation temperature), followed by being “set” in the stretched configuration by cooling the material while substantially retaining the stretched dimensions. Upon subsequently heating unrestrained, unannealed, oriented polymer-containing material to its orientation temperature, heat shrinkage is produced almost to the original unstretched, i.e., pre-oriented dimensions. More particularly, the term "oriented”, as used herein, can refer to oriented films, wherein the orientation can be produced in one or more of a variety of manners.
- packaging refers to packaging materials configured around a product being packaged, and can include (but are not limited to) bags, pouches, trays, and the like.
- the term "polymer” refers to the product of a polymerization reaction, and can be inclusive of homopolymers, copolymers, terpolymers, etc.
- the layers of a film can consist essentially of a single polymer, or can have still additional polymers together therewith, i.e., blended therewith.
- proteolytic enzyme refers to an enzyme that can be added to a marinade fluid to sever peptide bonds in proteins, and therefore tenderize a meat.
- Proteolytic enzymes suitable for use with the presently disclosed subject matter can include, but are not limited to, bromelain from pineapple and papain from papaya, achromopeptidase, aminopeptidase, ancrod, angiotensin converting enzyme, bromelain, calpain, calpain I, calpain II, carboxypeptidase A, carboxypeptidase B, carboxypeptidase G, carboxypeptidase P, carboxypeptidase W, carboxypeptidase Y, caspase, caspase 1, caspase 2, caspase 3, caspase 4, caspase 5, caspase 6, caspase 7, caspase 8, caspase 9, caspase 10, caspase 11, caspase 12, caspase 13, cathepsin B, cathepsin
- protease from Bacillus polymyxa, protease from Bacillus sp, protease from Bacillus sp (Esperase), protease from Rhizopus sp., protease S, proteasomes, proteinase from Aspergillus oryzae, proteinase 3, proteinase A, proteinase K, protein C, pyroglutamate amiopeptidase, renin, rennin, streptokinase, subtilisin, thermolysin, thrombin, tissue plasminogen activator, trypsin, tryptase, urokinase, and combinations thereof.
- the term "rupturable" with regard to a seal can indicate the susceptibility of being broken without implying weakness.
- a rupturable seal between the films of a package it can be meant that when so sealed the films are united together in a fluid impervious manner, and when the seal is broken or severed by delamination of the films from one another in the area of the seal, the films are separated apart from one another severing the seal while still maintaining the integrity of the individual films themselves.
- the rupturable seal in an intact state serves to maintain the integrity of the product chamber reservoir for maintaining fluid, semi-fluid, and/or solid products therein but in a broken or severed state allows for passage of these products between the films along a delaminated seal area.
- the term "seal" refers to any seal of a first region of an outer film surface to a second region of an outer film surface, including heat or any type of adhesive material, thermal or otherwise.
- the seal can be formed by heating the regions to at least their respective seal initiation temperatures.
- the sealing can be performed by any one or more of a wide variety of means, including, but not limited to, using a heat seal technique (e.g., melt-bead sealing, thermal sealing, impulse sealing, dielectric sealing, radio frequency sealing, ultrasonic sealing, hot air, hot wire, infrared radiation, etc.).
- a heat seal technique e.g., melt-bead sealing, thermal sealing, impulse sealing, dielectric sealing, radio frequency sealing, ultrasonic sealing, hot air, hot wire, infrared radiation, etc.
- the phrases “seal layer”, “sealing layer”, “heat seal layer”, and “sealant layer”, refer to an outer film layer, or layers, involved in the sealing of the film to itself, another film layer of the same or another film, and/or another article that is not a film. It should also be recognized that in general, up to the outer 3 mils of a film can be involved in the sealing of the film to itself or another layer. With respect to packages having only fin-type seals, as opposed to lap-type seals, the phrase “sealant layer” generally refers to the inside film layer of a package, as well as supporting layers adjacent this sealant layer often being sealed to itself, and frequently serving as a food contact layer in the packaging of foods.
- a sealant layer sealed by heat-sealing layer comprises any thermoplastic polymer.
- the heat-sealing layer can comprise, for example, thermoplastic polyolefin, thermoplastic polyamide, thermoplastic polyester, and thermoplastic polyvinyl chloride.
- the heat-sealing layer can comprise thermoplastic polyolefin.
- thermoforming layer refers to a film layer that can be heated and drawn into a cavity while maintaining uniform thinning, as opposed to films or film layers that lose integrity during the thermoforming process (e.g., polyethylene homopolymers do not undergo thermoforming with uniform thinning).
- thermoforming layers can comprise, but are not limited to, polyamide, ethylene/propylene copolymer, and/or propylene homopolymer; in some embodiments, nylon 6, nylon 6/6, amorphous nylon, ethylene/propylene copolymer, and/or propylene homopolymer.
- thermoplastic refers to uncrosslinked polymers of a thermally sensitive material that flow under the application of heat or pressure.
- tie layer refers to any internal layer having the primary purpose of adhering two layers to one another.
- tie layers can comprise any nonpolar polymer having a polar group grafted thereon, such that the polymer is capable of covalent bonding to polar polymers such as polyamide and ethylene/vinyl alcohol copolymer.
- tie layers can comprise at least one member selected from the group including, but not limited to, modified polyolefin, modified ethylene/vinyl acetate copolymer, and/or homogeneous ethylene/alpha-olefin copolymer.
- tie layers can comprise at least one member selected from the group consisting of anhydride modified grafted linear low density polyethylene, anhydride grafted low density polyethylene, homogeneous ethylene/alpha-olefin copolymer, and/or anhydride grafted ethylene/vinyl acetate copolymer.
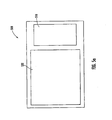
- FIG. 1 illustrates a package assembly 100 consistent with an exemplary embodiment of the present invention.
- the package assembly 100 contains at least a first package 200 and a second package 300.
- the first package 200 may contain two or more compartments.
- a first compartment 225 may substantially contain the second package 300 and a second compartment 230 may substantially contain one or more food products 110, such as a meat.
- the second package 300 may contain one or more food additives 120, such as a marinade.
- the second package 300 is substantially contained in the first compartment 225 of the first package, the second package 300 may include a reputable seal 350a located proximate the second compartment 230.
- applying pressure to at least the first compartment 225 and, thus, the second package 300 may break the rupturable seal 310 to distribute the food additive 120 from the second package 300 to the food product 110 in the second compartment 230 of the first package.
- the first package 200 may include a perimeter hard seal 235 configured to withstand the applied pressure and, thus, prevent the leaking of any of the food product 110 or the food additive 120 from the first package during the distribution of the food additive 120.
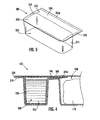
- FIG 2 illustrates an example of a first package 200 without the second package, any food additives or food products.
- the first package 200 can be fabricated from a first film 215 that is extruded and thermoformed to produce the first compartment 225 and the second compartment 230.
- the first and second compartments are separated from another by a partition 240 defined by two inner walls of the compartments 225 and 230.
- a second thermoplastic film 220 can be hermetically sealed to first thermoplastic film 215 through a perimeter seal 235 such that the compartmented first package 200 is substantially air and liquid tight.
- the perimeter seal 235 extends around the perimeter of first package 200 to create an airtight container.
- the first film 215 and/or the second film 220 can be transparent so that the contents of the first package can be viewed.
- the first package may be include a secondary seal (not illustrated) to provide additional strength to one or more compartments of the first package as further disclosed in U.S. Patent Application Serial No. 12/079,409 filed on March 26, 2008 (entitled “On-Demand Meat Tenderizing Package”; Attorney Docket No. D-44119-01) and assigned to the assignee of the present application.
- the perimeter seal 235 can be used to reliably contain the second package 300 containing the food additive and the food product in their respective compartments at normal operating pressures before, during, and after marinating.
- the perimeter seal 235 can also provide a margin of safety to contain the contents of the first package 200 in the event that the first package is dropped, bumped, and/or otherwise transiently exposed to higher pressures either before the rupturable seal 350 of the second package is broken or afterwards.
- the perimeter seal 235 (and/or, in embodiments having a secondary seal, the secondary seal) can be configured to be a hard or permanent seal in that the strength of the seal is intended to be strong enough to prevent rupture or the strength of the seal is intended to be equal to or higher than the strength of the sealed plastic films 215 and 220.
- Figures 1 and 2 illustrate that the first package 200 can be closed on all four edges.
- one or more of the edges can comprise sealed edges.
- the first package may be formed by heat sealing films 215 and 220 to form a package containing a second package and a food product in the first and second compartments 225 and 230.
- the heat sealing operation can occur at the food packaging plant using a heat sealing machine designed for high speed operation. Heat sealing can occur by any of a number of techniques well known in the art, such as but not limited to, thermal conductance heat sealing, impulse sealing, ultrasonic sealing, dielectric sealing, and/or combinations thereof.
- the heat sealing machine includes a heated seal bar that contacts and compresses the two films to be heat sealed together to form the perimeter seal 235.
- the seal bar temperature can refer to the surface temperature of the seal bar.
- the dwell time can refer to the length of time that the heated seal bar contacts the film to transfer heat from the seal bar to soften at least a portion of the films ( e.g ., the sealing layers of the films) so that they can be melded together.
- the sealing pressure can refer to the amount of force that squeezes the films together during this heat transfer. All of these variables can be modified accordingly in order to prepare a package suitable with the presently disclosed subject matter.
- the heat sealing machines present in food packaging plants can be designed and set to operate with a seal bar temperature, a dwell time, and a sealing pressure in a range useful for such materials to permit the heat sealing machines to operate at high speeds to form strong seals.
- the films of presently disclosed package 200 may be heat-sealed to form perimeter seal 235
- the use of other adhesives or mechanical closures e.g ., clips
- adhesives can be applied in a desired pattern, or sealed at a certain temperature (such as with a layer of ionomer) to define seal strength in a directly proportional fashion; i.e ., more adhesive or higher temperature can create a stronger seal, while less adhesive or lower temperature can produce a weaker seal.
- the perimeter seal 235 may not be sealed until after the first package 200 is filled.
- the first film 215 is formed into a compartmented support member having at least two compartments adapted to contain a second package and a food product.
- the compartmented support member is then loaded with a second package containing the food additive and the food product.
- the second film 220 can be positioned to contact the first film 215 at least along the perimeter of the first package.
- a vacuum can then be applied to the compartments.
- the second film 220 can then be sealed around the perimeter of the compartmented support member to form the perimeter seal 235 in this regard the second film 220 can function as a cover to the support member.
- FIG. 3 illustrates an example of a second package 300 without any food additives.
- the second package 300 can be fabricated similar to the first package 200 as described in the above exemplary embodiment in that two films may be sealed together along four edges to form a package.
- the second package can include a first film that is folded unto itself such that the fold in the first film forms an edge of the package and the remaining edges may be sealed together.
- the second package 300 can be fabricated from the first film 315 that is extruded and thermoformed to produce a compartment 325 and a first part 350 of a flange extending away from the compartment 325.
- the second film 320 can be hermetically sealed to first thermoplastic film 315 through a perimeter seal 335 such that the compartment 325 is substantially air and liquid tight.
- the perimeter seal 335 extends substantially around the perimeter of the second package 300 to create an airtight container.
- the second film 320 may also define a second part 355 of the flange that corresponds to the first part 350.
- the perimeter seal 335 or another seal may be used to seal the first and second parts 350 and 355 together and the sealed first and second parts define a flange 360 of the second package.
- the first film 315 and the second film 320 can be transparent so that the contents of the second package 300 can be viewed.
- the second package 300 or, more particularly, the compartment 325 of the second package 300 may be configured to substantially fit into and, thus, be contained in the first compartment 225 of first package 200. Therefore, the second package 300 can be adapted to be slightly smaller than the first compartment of the first package 200.
- Figures 1 and 3 illustrate that the second package 300 can be closed on all four edges.
- one or more of the edges can comprise sealed edges.
- the second package is formed from two separate sheets of plastic film, the four edges may all be sealed edges.
- the second package 300 can be formed by heat sealing the two films 315 and 320 to form an airtight container.
- the heat sealing operation can occur at the food packaging plant (however, not necessarily at the same food packaging plant as for the first package) using a heat sealing machine designed for high speed operation. Heat sealing can occur by any of a number of techniques well known in the art, such as but not limited to, thermal conductance heat sealing, impulse sealing, ultrasonic sealing, dielectric sealing, and/or combinations thereof.
- the heat sealing machine includes a heated seal bar that contacts and compresses the two films to be heat sealed together to form the perimeter seal 335.
- the seal bar temperature can refer to the surface temperature of the seal bar.
- the dwell time can refer to the length of time that the heated seal bar contacts the film to transfer heat from the seal bar to soften at least a portion of the films ( e.g ., the sealing layers of the films) so that they can be melded together.
- the sealing pressure can refer to the amount of force that squeezes the films together during this heat transfer. All of these variables can be modified accordingly in order to prepare a package suitable with the presently disclosed subject matter.
- the heat sealing machines present in food packaging plants can be designed and set to operate with a seal bar temperature, a dwell time, and a sealing pressure in a range useful for such materials to permit the heat sealing machines to operate at high speeds to form strong seals.
- the films of the second package 300 may be heat-sealed to form the perimeter seal 335
- other adhesives or mechanical closures e.g ., clips
- adhesives can be applied in a desired pattern, or sealed at a certain temperature (such as with a layer of ionomer) to define seal strength in a directly proportional fashion; i.e., more adhesive or higher temperature can create a stronger seal, while less adhesive or lower temperature can produce a weaker seal.
- the perimeter seal 335 may not be sealed until after the second package 300 is filled.
- the first film 315 can be formed into a support member having a compartment 325 adapted to contain a food additive and a defining a first part 350 of a flange.
- the compartment 325 may then be loaded with a food additive.
- the second film 320 can be positioned to contact the first film 315, at least, along the perimeter of the second package.
- a vacuum can then be applied to the compartment 325.
- the second film 320 can then be sealed around the perimeter of the support member to form perimeter seal 335.
- the second film 320 can function as a cover that is sealed to the support member.
- the filling of the food additive into the second package and the sealing of the second package may incur before or after the second package is placed into the first compartment of the first package.
- the filing and sealing operations of the second package may incur before the introduction of the first package.
- the filing and sealing operations may incur at a different location or even facility than the forming and sealing of the first package.
- Such an embodiment may reduce the likelihood of cross-contamination of the food additive and the food product.
- the perimeter seal 335 or one or more portions thereof may be designed to break when exposed to a predetermined pressure, referred to as being rupturable.
- the rupturable perimeter seal 335 of the second package is particularly configured to have a lower rupture pressure compared to perimeter hard seal 235 (and, in embodiments having a secondary seal, the secondary seal) of the first package such that the seal(s) of the first package is unaffected by the rupture of perimeter rupturable seal 335 of the second package.
- perimeter rupturable seal 335 may be configured to rupture in a controlled manner across a sufficient area to provide a relatively low-pressure movement of a flowable food additive (such as marinade) out of the compartment 325 of the second package.
- the perimeter seal of the second package may be configured to rupture
- the perimeter seal may have only a portion that is configured to rupture, e.g., the portion extending across the flange or, more specifically, the second package may include a first permanent seal that extends around the perimeter except for the portion extending across the flange and a second rupturable seal that extends across the flange.
- the second rupturable seal when pressure is applied, the second rupturable seal is intended to rupture before the first permanent seal and, thus, the food additives would escape through the flange only.
- a rupturable seal can be formed by any of a number of various techniques known in the art. Particularly, it will be understood that there are a number of ways of making a rupturable seal in accordance with the presently disclosed subject matter, including, but not limited to, one or more of zone patterning, adhesive, ultrasonic welding, thermal bonding, crimping, cohesives, compression, nipping, needle punching, sewing, hydroentangling, and the like.
- rupturable seal can be formed of a pattern of printed ink that prevents the package films from heat sealing at an inked portion, such that the amount of inked portions in the ink pattern determine the strength of the seal.
- rupturable seal can be fabricated by means of a discontinuity within the seal width.
- one discontinuity within rupturable seal can include one or more stress concentrators having an inflection point that is more responsive to the interior bag pressure force than other portions that are relatively straight or smoothly curved.
- a rupturable seal can be comprised of incompatible polymer blends.
- each of the films 315 and 320 can be fabricated from an extrusion molding process in which two or more thermoplastic materials or polymer blends are melted and extruded together.
- One or more of the thermoplastic materials may be incompatible to each other such that the addition of the one or more of the thermoplastic materials increases the resistance of the two films 315 and 320 to seal together due to the incompatible materials in the films 315 and 320.
- the seal strengths of rupturable seal can depend on the particular polymer blend used.
- common polymer blends can include, but are not limited to, zinc neutralized ethylene-acid (EMAA or EAA) copolymer ionomer (e.g., Surlyn 1650) with ethylene vinyl acetate (EVA) copolymer (e.g., Elvax 3120) and optionally with or without polybutylene; polypropylene with ethylene vinyl acetate; sodium neutralized EMAA, EMAA, and/or EVA; EVA and polystyrene or polystyrene copolymer (e.g., K-Resin® or Styralux®); and/or EVA with polybutylene.
- EVA zinc neutralized ethylene-acid
- EAA ethylene vinyl acetate copolymer
- EVA ethylene vinyl acetate copolymer
- EVA polypropylene with ethylene vinyl acetate
- the strength of a rupturable seal can be manipulated by the temperature, dwell time and/or pressure of the heat seal bar, depending on the type and thickness of the sealant being applied. It is to be understood that the pressure required to a separate rupturable seal can depend upon the width of the sealed area at the inner end thereof. Thus, the size and configuration of rupturable seal can be altered to vary the pressure within the sealed enclosure required to rupture the seal.
- the second package 300 is substantially contained in the first compartment 225 of the first package 200.
- the flange 360 of the second package extends from the first compartment 225 of the first package toward the second compartment 230 of the first package. More specifically, the flange 360 extends from the first compartment 225 at least partially across the partition 240 separating the first and second compartments 225 and 230 into the second compartment 230 such that the second package 300 is in fluid communication with the second compartment 230 when the rupturable seal 335a across the flange 360 ruptures.
- the food additive 120 in the second package 300 may leave the second package 300 via the flange 360 into the second compartment 230 and interact with the food product 120 contained in the second compartment 230.
- the perimeter hard seal 235 of the first package is configured to prevent any of the food additive 120 or food product 110 from leaking out of the first package 200.
- first package and the second package can be manufactured through an extrusion molding and thermoform molding process.
- first package 200 can be fabricated from the first film 215 that is extruded and thermoformed to produce the first compartment 225 and the second compartment 230.
- Extrusion molding is well known plastic shaping processing in which, e.g ., thermoplastic material are fed from a hopper or other device into an extruder configured to heat the thermoplastic material and force it through a die to form and particular profile such as a plastic film or sheet.
- Thermoforming is well known in the packaging art, and is the process whereby a thermoplastic web is heat softened and reshaped to conform to the shape of a cavity in a mold.
- thermoforming methods include a vacuum forming or plug-assist vacuum forming method.
- a vacuum forming method the first web is heated, for example, by a contact heater, and a vacuum is applied beneath the web causing the web to be pushed by atmospheric pressure down into a preformed mold.
- a plug-assist vacuum forming method after the first or forming web has been heated and sealed across a mold cavity, a plug shape similar to the mold shape impinges on the forming web and, upon the application of vacuum, the forming web transfers to the mold surface.
- first film 215 of the first package may be considered a "bottom" web, e.g ., in normal usage, the first package can rest on the first film 215 such that the web comprises the bottom of first package 200.
- the second film 200 may be considered a "top” web, e.g ., in normal usage, the first package can be positioned such that the web of the second film comprises the top of the first package that covers the bottom web.
- first package may be manufactured, stored, shipped, and/or displayed in any suitable orientation.
- the first package may be placed on a supporting surface such that the thermoformed web functions as the top of the package and the covering web functions as the bottom of the package.
- the first and second films 215 and 220 of the first package may be multilayered structures having various layers that are produced using coextrusion techniques and lamination techniques well known in the art.
- the films can be coextruded or laminated and can be adhered together with a coextruded tie layer such as ethylene vinyl acetate, an ionomer, anhydride grafted ethylene vinyl acetate, low density polyethylene and/or linear low density polyethylene.
- the typical film-to-film bond from lamination may be made by adhering the films together with a thin layer of polyurethane coating on an adhesive laminator.
- the lamination can also be accomplished by extrusion lamination or extrusion coating with an adhesive coextrusion tie layer type resin at the bond interface.
- films of the presently disclosed subject matter can be manufactured by coextrusion methods and adhesive lamination methods, such as those disclosed in U.S. Patent No. 6,769,227 to Mumpower , the content of which is incorporated herein in its entirety by reference thereto. Accordingly, films of the presently disclosed subject matter can be made by any suitable process, including coextrusion, lamination, extrusion coating, and combinations thereof.
- the films used to form the disclosed packages can be provided in sheet or film form and can be any of the films commonly used for this type of packaging. In some embodiments, however, the film can be a commercially available multilayer film having a sealant layer, a barrier layer, and one or more abuse layers.
- the first and second films of the first package may comprise one or more barrier layers.
- barrier layers can include, but are not limited to, ethylene/vinyl alcohol copolymer, polyvinylidene chloride, polyalkylene carbonate, polyamide, polyethylene naphthalate, polyester, polyacrylonitrile, and combinations thereof, as known to those of skill in the art.
- the barrier layer can comprise either EVOH or polyvinylidene chloride, and the PVDC can comprise a thermal stabilizer (i.e., a HCl scavenger, such as epoxidized soybean oil) and/or a lubricating and/or processing aid, which are well known in the art.
- the first and second films of the first package may comprise one or more seal layers.
- seal layers can include, but are not limited to, the genus of thermoplastic polymers, including thermoplastic polyolefin, polyamide, polyester, polyvinyl chloride, homogeneous ethylene/alpha-olefin copolymer, ethylene/vinyl acetate copolymer, ionomer, and combinations thereof.
- the first and second films of the first package may comprise one or more tie layers.
- tie layers can comprise any nonpolar polymer having a polar group grafted thereon, so that the polymer is capable of covalent bonding to polar polymers, such as polyamide and ethylene/vinyl alcohol copolymer.
- tie layers can comprise at least one member of the group including, but not limited to, modified polyolefin, modified ethylene/vinyl acetate copolymer, homogeneous ethylene/alpha-olefin copolymer, and combinations thereof.
- tie layers can comprise at least one member selected from the group including, but not limited to, anhydride modified grafted linear low density polyethylene, anhydride grafted low density polyethylene, homogeneous ethylene/alpha-olefin copolymer, and/or anhydride grafted ethylene/vinyl acetate copolymer.
- the first and second films of the first package may comprise one or more abuse layers.
- abuse layers can comprise any polymer, so long as the polymer contributes to achieving an integrity goal and/or an appearance goal.
- the abuse layer can include, but is not limited to, polyamide, ethylene/propylene copolymer, nylon 6, nylon 6/6, amorphous nylon, and combinations thereof.
- the first and second films of the first package may comprise one or more bulk layers to increase the abuse-resistance, toughness, modulus, etc., of the film.
- the bulk layer can comprise polyolefin, including but not limited to, at least one member selected from the group consisting of ethylene/alphaolefin copolymer, ethylene/alpha-olefin copolymer plastomer, low density polyethylene, and linear low density polyethylene.
- the polymer components used to fabricate the films according to the presently disclosed subject matter can also comprise appropriate amounts of other additives normally included in such compositions.
- slip agents such as talc
- antioxidants such as talc
- fillers such as talc
- dyes such as pigments and dyes
- radiation stabilizers such as UV stabilizer
- antistatic agents such as elastomers, and the like
- the films employed in the presently disclosed subject matter can be multilayer or monolayer, although, of course, those films defined as delaminatable, multilayer films must include at least two layers.
- the films employed will have two or more layers in order to incorporate a variety of properties, such as, for example, sealability, gas impermeability and toughness, into a single film.
- At least a portion of at least one film of the presently disclosed subject matter can be irradiated to induce cross-linking.
- the film is subjected to one or more energetic radiation treatments, such as corona discharge, plasma, flame, ultraviolet, X-ray, gamma ray, beta ray, and high energy electron treatment, each of which induces cross-linking between molecules of the irradiated material.
- energetic radiation treatments such as corona discharge, plasma, flame, ultraviolet, X-ray, gamma ray, beta ray, and high energy electron treatment, each of which induces cross-linking between molecules of the irradiated material.
- Films of the presently disclosed subject matter can have any total thickness desired, so long as the films provide the desired properties for the particular packaging operation in which the film is used.
- Final web thicknesses can vary, depending on process, end use application, and the like. Typical thicknesses range between 0.0025 to 0.51 mm (0.1 to 20 mils), in some embodiments between 0.0076 and 0.38 mm (0.3 and 15 mils), in some embodiments 0.013 to 0.25 mm (0.5 to 10 mils), in some embodiments 0.025 to 0.20 mm (1 to 8 mils), in some embodiments 0.076 to 0.15 mm (3 to 6 mils), such as 0.10 to 0.13 mm (4 to 5 mils).
- top webs can have a thickness of between 0.05 and 0.13 mm (2 and 5 mils), and bottom webs can have a thickness of between 0.13 and 0.25 mm (5 and 10 mils).
- the film according to the presently disclosed subject matter comprises a total of from about 4 to about 20 layers; in some embodiments, from about 4 to about 12 layers; and in some embodiments, from about 5 to about 9 layers.
- the disclosed film can comprise 1, 2, 3, 4, 5, 6, 7, 8, 9, 10, 11, 12, 13, 14, 15, 16, 17, 18, 19, or 20 layers.
- the film of the disclosed package can have any total thickness desired, so long as the film provides the desired properties for the particular packaging operation in which the film is used, e.g. optics, modulus, seal strength, and the like.
- first and second films of the first package may be transparent (at least in the non-printed regions) so that the packaged articles are visible through the films.
- Transparent as used herein means that the material transmits incident light with negligible scattering and little absorption, enabling objects (e.g., packaged food or print) to be seen clearly through the material under typical unaided viewing conditions (i.e., the expected use conditions of the material).
- the transparency (i.e., clarity) of the film can be at least about any of the following values: 20%, 25%, 30%, 40%, 50%, 65%, 70%, 75%, 80%, 85%, and 95%, as measured in accordance with ASTM D1746.
- the seals can be formed using a heat sealing machine that includes a heated seal bar that contacts and compresses films together to form a seal.
- a heated seal bar that contacts and compresses films together to form a seal.
- the heating bar can then be removed to allow the sealed area to cool and form a sealed bond.
- the resulting perimeter seal 235 can extend continuously around the outside edge of package 200 to hermetically seal or enclose the food product and/or the second package and thus food additive housed therein.
- first and second films 215 and 220 of the first package can form a substantially gas-impermeable enclosure to protect the food product and the second package from contact with the surrounding environment including atmospheric oxygen, dirt, dust, moisture, liquid, microbial contaminates, and the like.
- the food product and the food additive contained in the second package can be packaged in a modified atmosphere package to extend the shelf life or bloom-color life.
- the resulting perimeter seal 235 between first and second films 215 and 220 may be sufficiently strong to withstand the expected use conditions.
- the bond strength of perimeter seal 235 can be at least about any of the following values: 7.0, 8.0, 9.0, and 10 pounds/inch or greater.
- the term "heat seal bond strength" as used herein can refer to the amount of force required to separate the second film 220 from first film 215, as measured in accordance with ASTM F88-94 where the Instron tensile tester crosshead speed is 5 inches per second, using five, 1-inch wide representative samples.
- the strength of the perimeter seal may be equal to or greater than the strength of the films themselves or otherwise be considered permanent or a hard seal.
- the rupturable seal 335a of the second package may be formed by any of a number of various techniques. Particularly, it will be understood that the rupturable seal 335a can be made using one or more of incompatible materials, zone patterning, adhesive, ultrasonic welding, thermal bonding, crimping, cohesives, compression, nipping, needle punching, sewing, hydro-entangling, and the like. A combination of these methods can also be used.
- the rupturable seal 335a of the second package is configured to have a lower strength than the perimeter seal 235 of the first package and of any of the films of the second package.
- the strength of the rupturable seal 335a can be any of the following values 1.0, 2.0, 3.0. 4.0, 5.0, 6.0, 7.0, and 8.0 pounds/inch.
- the processes may include a horizontal form, fill and seal machine, e.g ., as partially shown in Figures 5a , 5b and 6 .
- Figure 5a illustrates a die box 500 for forming the compartmented support member of the first package.
- the die box 500 includes a first cavity 510 for forming the first compartment and second cavity 520 for forming the second compartment.
- a sheet of film may be placed against the die box and the first and second compartments may be formed through a thermoforming process in which portions of the sheet of film are forced (through a plug and/or vacuum force) to assume the shape of the two cavities.
- the same die box 500 can be modified to form one or more second packages according to the exemplary embodiments described herein.
- inserts may be used to modify the cavities to form compartments of the second packages rather than the first and second compartments of the first package. More specifically and as illustrated in Figure 5b , a first insert 610 may be placed into the first cavity 510 such that the first insert 610 defines a modified first cavity 615 of the die box having a size slightly smaller than the unmodified first cavity 510. The intent of modifying the first cavity is to form a compartment of the second package that is slightly smaller than the first compartment of the first package and, thus, allow the compartment of the second package to fit into the first compartment.
- a second insert 620 may be placed into the second cavity 520. The second insert 620 defines two cavities, referred to as a second cavity 625 and a third cavity 630.
- Each of the second cavity 625 and third cavity 630 is substantially the same as the modified first cavity 615 such that each of the second cavity and the third cavity form substantially the same size compartment as the modified first cavity.
- a sheet of film may be placed against the die box 500 and three compartments may be formed through an extrusion process in which portions of the sheet of film are forced (through a plug and/or vacuum force) to assume the shape of the cavities.
- the food additives may be added to each of the compartments, a second sheet of film may be placed onto and sealed with the first sheet of film and compartments.
- a vacuum process may also be used to evacuate the atmosphere in the compartments prior to sealing the films together.
- the first and second sealed films may be trimmed or cut to form three packages containing a food additive.
- the cutting operations may be used to define a flange of each package.
- the flange can be used as conduit between the first and second compartments of the first package.
- Figure 6 illustrates the second package 300 placed in a first compartment 225 of a formed support member 215 of the first package.
- a flange 360 of the second package extends at least partially across the partition 240 separating the first and second compartments 225 and 230.
- a food product (not illustrated in Figure 6 ) may be placed into the second compartment.
- a second sheet of film or a cover may be placed onto and sealed with the support member and its compartments.
- a vacuum process may also be used to evacuate the atmosphere in the compartments prior to sealing them.
- the second sealed film or cover may be trimmed or cut to correspond to the bottom support member of the first package.
- a second seal and a third seal may be applied to the first package.
- a second seal may be applied between the first plastic film of the first package and the first plastic film of the second package that corresponds to the flange of the second package.
- a third seal may be applied between the second plastic film of the second package and the second plastic film of the second package that corresponds to the flange of the second package.
- the second and third seals can be either a hard seal or rupturable seal. The intent of the second and third seals is to prevent the food product from leaking from the second compartment to the first compartment prior to the rupturing of the rupturable seal of the second package.
- the second compartment 230 of the first package 200 may comprise a food product, such as a cut of meat.
- meat that are suitable for use with the presently disclosed subject matter can include, but are not limited to, beef, birds such as poultry (including chicken, duck, goose, turkey, and the like), buffalo, camel, crustacean (including shellfish, clams, scallops, mussels, oysters, lobster, crayfish, crab, shrimp, prawns, and the like), dog, fish (including salmon, trout, eel, cod, herring, plaice, whiting, halibut, turbot, ling, squid, tuna, sardines, swordfish, dogfish, shark, and the like), game (including deer, eland, antelope, and the like), game birds (such as pigeon, quail, doves, and the like), goat, hare, horse, kangaroo, lamb, marine mammals (including whales
- meat substitutes can be used and are included under the term "meat". Such meat substitutes can approximate the aesthetic qualities and/or chemical characteristics of certain types of meat.
- the meat substitutes can include, but are not limited to, herean, rice, mushrooms, legumes, tempeh, textured vegetable protein, soy concentrate, mycoprotein-based Quorn, modified defatted peanut flour, and/or pressed tofu to make the meat substitute look and/or taste like chicken, beef, lamb, ham, sausage, seafood, and the like.
- the food product can comprise one or more vegetables.
- Vegetables that are particularly suited for use with the presently disclosed subject matter can include, but are not limited to, artichokes, asparagus, beans, bean sprouts, beets, broccoli, cauliflower, cabbage, carrots, celery, corn, collards, eggplant, green peppers, kale, leeks, mushrooms, mustard greens, onions, peas, potatoes, radishes, red peppers, rhubarb, spinach, squash, sweet potatoes, turnips, water chestnuts, watercress, yarns, yellow peppers, and/or zucchini.
- the vegetable can be diced, minced, shaved, and/or cut into strips.
- the food product suitable for use with the presently disclosed subject matter is not particularly limited.
- the presently disclosed methods and package can be applied to raw (i.e., uncooked) food products, partially cooked food products, and/or pre-cooked products, where the cooking process is intended to cook, completely cook, and/or re-heat the food product.
- the food product selected can be any type that is suitable for consumption.
- the food product can be non-rendered, non-dried, raw, and can comprise mixtures of whole muscle meat formulations. Whole meat pieces can be fresh, although frozen or semi-frozen forms can also be used. Since freezing affects the tenderness of meat by rupturing intrafibrillar tissue as a result of ice crystal formation, the increased tenderness resulting from freezing can be taken into account when using such products in the package and methods described herein.
- the first compartment 225 of the first package 200 can substantially contain a second package 300 which may house a food additive, such as marinade.
- a food additive such as marinade.
- the amount of marinade to be used in the presently disclosed subject matter depends on the type and added amount of food additive.
- the food additive can be in any form including, but not limited to, liquid, paste, powder, and/or combinations thereof.
- the food additive can be in the form of liquid or powder from the standpoint of handleability, preservability, and the like. If the food additive of the presently disclosed subject matter is used in liquid form, it can be in the form of solution or dispersion in water or an aqueous liquid or in the form of solution or dispersion in fatty oil.
- the food additive can be frozen when added to package in order to allow heat sealing mechanisms to function appropriately. That is, when a liquid food additive is added to package, the liquid nature of the food additive can interfere with the heat sealing process, producing a non-hermetic seal.
- the food additive can comprise one or more enzymatic tenderizers to form a tenderized meat product.
- one or more proteolytic enzymes can be added to the food additive to sever peptide bonds in proteins, and therefore tenderize the meat.
- Proteolytic enzymes suitable for use with the presently disclosed subject matter can include, but are not limited to, bromelain from pineapple and papain from papaya, achromopeptidase, aminopeptidase, ancrod, angiotensin converting enzyme, bromelain, calpain, calpain I, calpain II, carboxypeptidase A, carboxypeptidase B, carboxypeptidase G, carboxypeptidase P, carboxypeptidase W, carboxypeptidase Y, caspase, caspase 1, caspase 2, caspase 3, caspase 4, caspase 5, caspase 6, caspase 7, caspase 8, caspase 9, caspase 10, caspase 11, caspase 12, caspase 13, cathepsin B, cathepsin C, cathepsin D, cathepsin G, cathepsin H, cathepsin L, chymopapain, chymase, chymotry
- protease from Bacillus polymyxa, protease from Bacillus sp, protease from Bacillus sp (Esperase), protease from Rhizopus sp., protease S, proteasomes, proteinase from Aspergillus oryzae, proteinase 3, proteinase A, proteinase K, protein C, pyroglutamate amiopeptidase, renin, rennin, streptokinase, subtilisin, thermolysin, thrombin, tissue plasminogen activator, trypsin, tryptase, urokinase, and combinations thereof.
- the food additive can comprise additional components, including but not limited to, bactericides, fungicides or other preservatives, wetting agents (e.g ., a Tween), antioxidants, viscosity control agents (e.g ., gums), brine ( e.g ., sodium chloride, phosphates, dextrose), curing agents ( e.g ., nitrites, sugars, erythorbate), flavoring agents ( e.g ., herbs, spices, and liquid smoke), and the like.
- wetting agents e.g a Tween
- antioxidants e.g a Tween
- viscosity control agents e.g ., gums
- brine e.g ., sodium chloride, phosphates, dextrose
- curing agents e.g ., nitrites, sugars, erythorbate
- flavoring agents e.g ., herbs, spices, and liquid smoke
- the second package 300 can be prepared such that the first film 315 of the second package can be formed into a compartment 325.
- a food additive 120 e.g ., a marinade
- the second film 320 can hermetically seal the food additive 120 within the second package 300.
- the first package 200 can be prepared such that first film 215 of the first package can be formed into first and second compartments 225 and 230.
- a food product 110 e.g., a meat
- the second package 300 containing the food additive 120 can be placed in the first compartment 230.
- the second package 300 can first be placed into the first compartment 225 of the first package and then the food additive 120 can be placed into the second package 300.
- the second film 220 of the first package can hermetically seal the food product 110 and the second package 300 and, thus, the food additive 120 within the second package 300.
- the presently disclosed subject matter is directed to a package assembly 100 for marinating and/or heating a food product.
- the package assembly 100 includes a first package 200 and a second package 300 contained within the first package 200.
- each of the first and second package 200 and 300 package assembly can comprise a first thermoformed film 215 and 315 formed into a compartmented support member having one or more compartments (e.g ., the first package 200 may have a first compartment 225 and a second compartment 230 and the second package 300 may have a compartment 325) and a second thermoplastic film 220, 320 disposed on the thermoformed film 215, 315.
- a food additive 120 can be disposed in the compartment 325 of the second package and the second package 300 can be disposed in the first compartment 225 of the first package.
- a food product 110 can be disposed in the second compartment 230 of the second package.
- the first and second films 215, 220 of the first package can then be sealed together to form a perimeter seal 235 around the perimeter of the first package 200.
- the perimeter seal 235 of the first package may be a hard seal in that the seal is not intended to rupture ( e.g ., the strength of the seal may be at least equal to the strength of the first and second films.).
- the first and second films 315, 320 of the second package can be sealed together to form a perimeter seal 335 around the perimeter of the second package 300.
- At least a portion 335a of the perimeter seal of the second package can be a rupturable seal.
- the rupturable seal 335a is configured to rupture in response to applied pressure, e.g ., the strength of the seal 335a may be less than that of any of the films 215, 220, 315, 320 of the first and second package and less than the perimeter seal 235 of the first package.
- the flange 360 of the second package can extend from the first compartment 225 of the first package at least partially over a partition 240 between the first and second compartments 225, 230 of the first package toward the second compartment 230 of the first package such that the second package 300 is in fluid communication with the second compartment 230 of the first package when the rupturable seal 335a ruptures.
- a user can grip the package assembly 100, and using his or her thumbs or a hard object, emit pressure on the first compartment 225 of the first package and thus onto the second package 300 contained substantially therein.
- the rupturable seal 335a of the second package will fail, allowing the food additive 120 contained in the second package 300 to flow from the compartment 325 of the second package through the flange 360 of the second package and into the second compartment 230 of the first package to freely mix with the food product 110 stored in the second compartment 230 of the first package.
- the perimeter seal 235 of the first package is configured to be strong enough to minimize the likelihood that the perimeter seal 235 would rupture or otherwise leak during this process and thus the food additive 120 and the food product 110 are contained within the first package 200 even when the pressure is applied for the user.
- the user can shake or rotate the package assembly 100 to fully mix the food product 110 and the food additive 120.
- the package assembly 100 can then be marinated for a desired amount of time.
- the package assembly 100 can be incubated a sufficient time to allow the food product to tenderize to a desired amount.
- the presently disclosed subject matter is directed to a method of controlling the level of food additive imparted to a food product.
- the method may comprise forming a second package including thermoforming a first thermoplastic film of the second package into a compartmented support member having a compartment; forming a first package including thermoforming a first thermoplastic film of the first package a compartmented support member having at least two compartments; loading the compartment of the second package with a food additive; applying a vacuum to the compartment of the second package; sealing the compartment with a second thermoplastic film of the second package and defining a flange of the second package, wherein the sealing includes providing a rupturable seal across the flange; loading the second package into the first compartment of the first package such that the flange of the second package extends at least partially over a partition between the first and second compartments of the first package; loading a food product in the second compartment of the first package; applying a vacuum to at least the second compartment of the first package; and sealing the first and second compartments of the first package with a second thermoplastic film of the first package, wherein the sealing includes providing a hard seal around the perimeter of the first package.
- the use of a second package to contain the food additive may have one or more additional advantages.
- the loading of the food additive into a second package first may minimize the likelihood of any premature cross-contamination between the food additive and the food product.
- loading the food additive and the food product directly into compartments at the same time may require that the food additive be frozen to allow the machinery to advance rapidly as well as to prevent flashing of a liquid as the vacuum is applied to the food product. Freezing the food additive may be costly and require time and the maintenance of an environment below 0°F.
- the thawing of the food additive after the packaging operations may create condensation on the surface of the package which may create aesthetic issues and may transfer to any cardboard boxing packaging used in connection with the package and weaken the cardboard.
- the food additive may be handled as a liquid which may allow for more options for handling and flashing of the liquid may be eliminated because less vacuum may be needed to pull the surface air from the package. Also, using a liquid would eliminate the limitations of a frozen food additive as discussed above.
- the use of a second package for the food additive allows for the first package to be specifically configured to hold the food product and the second package to be specifically configured to hold the food additive.
- the materials of the first package can be "breathable" which may be preferred for food products such as fish or chicken and the materials of the second package may include barrier layers which may be preferred for the food additive.
- the second packages may be labeled or printed individually and then placed in a first package so a customer may change from one type to another type of food additive without changing the top web of film used for the first package even if it is printed for a particular food product.
- the use of the second package also allows for the seals to be specifically configured for particular functions.
- the perimeter seal of the first package may be a hard seal that reduces the likelihood of the first package rupturing or otherwise leaking even as the user applies pressure or shakes the package assembly to mix the food additive and food product, while the rupturable seal of the second package is specifically configured to rupture and allow the food additive and the food product to mix.
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Packages (AREA)
- Packging For Living Organisms, Food Or Medicinal Products That Are Sensitive To Environmental Conditiond (AREA)
Description
- Of the several sensory characteristics of meat, tenderness is perhaps the trait most highly desired by consumers. Consequently, meat tenderness is a factor of major economic importance to the livestock and meat industries. Accordingly, the consumer acceptance of meat, e.g., beef, pork and poultry, depends to a large measure on the tenderness of the meat after cooking. When the meat is tough and fibrous, consumer acceptance is quite low. Meat prepared for home consumption and sold in local groceries and butcheries is normally of the more tender grades. For example, in the case of beef, lot feeding can be required to develop the desired amount of tenderness in the muscle tissue, including increases in fat content. However, such efforts can considerably increase the cost of the meat. For this reason, significant effort has been expended in the art to provide methods for tenderizing less tender grades of meat.
- Commonly, food additives (such as, for example, marinades) can be used to enhance the qualities of meats by providing enhanced visual appearance and tenderness from spices and flavorings. For example, some techniques utilize injection of flavorings into the muscle to impart flavor and juiciness prior to packaging the meat. Other techniques include a means of tumbling a meat product in a marinade prior to packaging. In the case of the injected or tumbled marinade techniques, the use of a tenderizer is often omitted because the proteolytic enzyme associated with tenderizing agents can overly soften the meat, resulting in an unsatisfactory texture. The over-tenderizing results from prolonged contact time between the meat and the tenderizing agent as a consequence of the poor ability to control the exposure time during distribution. Additionally, even without considering the role of a proteolytic enzyme, the quality of a pre-marinated package is necessarily inconsistent as the meat generally is exposed for too long to the flavorants.
- Alternatively, restaurants or consumers can purchase a vacuum packaged meat package, cut open the package, and transfer the meat to a second bag wherein a marinade is added, or to a tray or vat that is loaded with a marinade. With the tray, vat, or second bag method, a consumer removes the meat from its shipment package and necessarily exposes the meat to outside conditions that can introduce contamination during marinating. In addition, the method can introduce the undesirable step of cleaning the tray or vat to prevent cross-contamination.
-
DE 20 2004 014511 U1 discloses a multi-chamber package comprising a base that forms a pair of wells separated by a rib, a first component may be placed in the well, while a second component can be placed in the well. A first film, which may be transparent and gas permeable, extends across the entirety of both wells and has a strong seal at the periphery of the package. A weaker seal is defined in the area of the rib between the two wells. A second film, which may be gas impermeable aluminium foil, extends across the opening of the well. When a user presses on the second film, the weaker seal releases such that the components mix. The transparency of the first film may allow the user to know when the components are fully mixed and ready for use. - FR
2 642 726 discloses a separate container for storing a first food item in a first compartment of a tray that cannot then be admixed with a second food item in a second compartment of the tray prior to opening the complete package assembly. - The presently disclosed subject matter provides, among other things, a package assembly that includes first and second packages that maintains two or more components, e.g., a food additive and a food product, separately until a user desires to mix the two components within the package assembly.
- The present invention provides a package assembly as defined in claim 1 essentially, comprising: a first package comprising a first compartment that substantially contains a second package and a second compartment configured to contain a food product; and the second package is configured to contain a food additive and includes a rupturable seal configured to rupture and allow the food additive to escape the second package when exposed to a predetermined pressure, wherein the second package is in fluid communication with the second compartment upon a rupturing of the rupturable seal so as to allow the food additive to mix with the food product, and wherein the first package is configured to withstand the predetermined pressure and prevent leaking of the food additive and food product from the first package during the mixing of the food additive and the food product.
- The present invention also provides a method of forming such a package assembly for controlling a level of food additive imparted to a food product as defined in claim 10, the method essentially comprising: forming a support member of a first package that includes a first compartment configured substantially to contain a second package and a second compartment configured to contain a food product; forming the second package configured to contain a food additive; loading the food additive into the second package; sealing the food additive in the second package with at least a rupturable seal configured to rupture and allow the food additive to escape the second package; loading the food product into the second compartment of the first package; loading the second package substantially into the first compartment of the first package such that the second package is in fluid communication with the second compartment of the first package upon a rupturing of the rupturable seal so as to allow the food additive to mix with the food product; and sealing the support member of the first package with a cover of the first package such that the first package is configured to withstand the predetermined pressure and prevent leaking of the food additive and food product from the first package during the mixing of the food additive and the food product.
- For example, according to an embodiment of the present invention, a package assembly for marinating a food product is provided.
- The first package may include a first plastic film and a second plastic film and the hard seal of the first package may extend around the perimeter of the first plastic film and the perimeter of the second plastic film. The first plastic film may be a thermoformed film formed into a compartmented support member having the first and second compartments.
- The second package may include a first plastic film and a second plastic film. The first plastic film may be a thermoformed film formed into a compartmented support member having a compartment. The first plastic film of the second package and the second plastic film of the second package may collectively form a flange of the second package extending away from the compartment and the rupturable seal may extend at least across the flange of the second package. As another example, the rupturable seal may extend around the perimeters of the first and second plastic films of the second package including across the flange.
- The first and second compartments of the first package may be separated by a partition and the flange of the second package may extend from the compartment of the second package at least partially across the partition toward the second compartment of the fist package.
- The package assembly may further include a seal between the flange and the first plastic film of the first package and a seal between the flange and the second plastic film of the first package.
- These and further embodiments, are defined in the dependent claims.
- The food additive may be selected from the group comprising: marinade, proteolytic enzyme, bactericide, fungicide, preservative, wetting agent, antioxidant, viscosity control agent, brine, curing agent, flavoring agent, and combinations thereof. The food product may be selected from the group comprising: meat, vegetable, and combinations thereof.
- The forming of the supporting member according to method claim 10 may include thermoforming a first plastic film of the first package. The forming of the second packaging may include thermoforming a first plastic film of the second package into a support member of the second package having a compartment of the second package. The loading the second package substantially into the first compartment of the first package may include positioning a flange of the second package at least partially across a partition separating the first compartment of the first package and the second compartment of the first package such that the flange extends from the first compartment of the first package toward the second compartment of the second package.
- Having thus described the invention in general terms, reference will now be made to the accompanying drawings, which are not necessarily drawn to scale, and wherein:
-
Figure 1 is a perspective view of a package assembly for on-demand marination according to an exemplary embodiment; -
Figure 2 is a is a perspective view of a first package of the package assembly ofFigure 1 without the second package having a food additive or a food product; -
Figure 3 is a perspective view of a second package of the package assembly ofFigure 1 without a food additive; -
Figure 4 is a cross-section view ofFigure 1 taken along line 4-4; -
Figure 5a is a top view of a die box consistent with an exemplary embodiment; -
Figure 5b is a top view of the die box ofFigure 5a modified through the use of two inserts; and -
Figure 6 is a top view of a second package placed into a first compartment of a formed support member of a first package. - The present inventions now will be described more fully hereinafter with reference to the accompanying drawings, in which some, but not all embodiments of the inventions are shown. Indeed, these inventions may be embodied in many different forms and should not be construed as limited to the embodiments set forth herein; rather, these embodiments are provided so that this disclosure will satisfy applicable legal requirements. Like numbers refer to like elements throughout.
- While the following terms are believed to be well understood by one of ordinary skill in the art, the following definitions are set forth to facilitate explanation of the presently disclosed subject matter.
- Unless defined otherwise, all technical and scientific terms used herein have the same meaning as commonly understood to one of ordinary skill in the art to which the presently disclosed subject matter belongs. Although any methods, devices, and materials similar or equivalent to those described herein can be used in the practice or testing of the presently disclosed subject matter, representative methods, devices, and materials are now described.
- Following long-standing patent law convention, the terms "a", "an", and "the" refer to "one or more" when used in the subject specification, including the claims. Thus, for example, reference to "a package" (e.g., "a marinade package") includes a plurality of such packages, and so forth.
- Unless otherwise indicated, all numbers expressing quantities of components, reaction conditions, and so forth used in the specification and claims are to be understood as being modified in all instances by the term "about". Accordingly, unless indicated to the contrary, the numerical parameters set forth in the instant specification and attached claims are approximations that can vary depending upon the desired properties sought to be obtained by the presently disclosed subject matter.
- As used herein, the term "about", when referring to a value or to an amount of mass, weight, time, volume, concentration, percentage, and the like can encompass variations of, in some embodiments ±20%, in some embodiments ±10%, in some embodiments ±5%, in some embodiments ±1%, in some embodiments ±0.5%, and in some embodiments ±0.1%, from the specified amount, as such variations are appropriate in the disclosed package and methods.
- As used herein, the phrase "abuse layer" refers to an outer film layer and/or an inner film layer, so long as the film layer serves to resist abrasion, puncture, and other potential causes of reduction of package integrity, as well as potential causes of reduction of package appearance quality. Abuse layers can comprise any polymer, so long as the polymer contributes to achieving an integrity goal and/or an appearance goal. In some embodiments, an abuse layer can comprise polymers having a modulus of at least 107 Pascals, at room temperature. In some embodiments, an abuse layer can comprise, but is not limited to, polyamide and/or ethylene/propylene copolymer; in some embodiments, nylon 6, nylon 6/6, and/or amorphous nylon.
- As used herein, the term "barrier", and the phrase "barrier layer", as applied to films and/or layers, can be used with reference to the ability of a film or layer to serve as a barrier to one or more gases. In the packaging art, oxygen (i.e., gaseous 02) barrier layers have included, for example, ethylene/vinyl alcohol copolymer (polymerized ethylene vinyl alcohol), polyvinyl chloride, polyvinylidene chloride (PVDC), polyalkylene carbonate, polyamide, polyethylene naphthalate, polyester, polyacrylonitrile, and the like, as known to those of ordinary skill in the art. In some embodiments, the 02-barrier layer can comprise ethylene/vinyl alcohol copolymer, polyvinyl chloride, polyvinylidene chloride, and/or polyamide.
- As used herein, the terms "corona treatment" and "corona discharge treatment" refer to subjecting the surfaces of thermoplastic materials, such as polyolefins, to corona discharge, i.e., the ionization of a gas such as air in close proximity to a film surface, the ionization initiated by a high voltage passed through a nearby electrode, and causing oxidation and other changes to the film surface, such as surface roughness. Corona treatment of polymeric materials is disclosed in
U.S. Patent No. 4,120,716, to Bonet .U.S. Patent No. 4,879,43 to Hoffman , discloses the use of corona discharge for the treatment of plastic webs for use in meat cook-in packaging, with the corona treatment of the inside surface of the web to increase the adhesion of the meat to the proteinaceous material. - As used herein, the term "film" can be used in a generic sense to include plastic web, regardless of whether it is film or sheet.
- As used herein, the term "food additive" refers to any liquid or solid material that results or can reasonably be expected to result, directly or indirectly, in its becoming a component or otherwise affecting the characteristics of any food product. In some embodiments, the food additive can, for example, be an agent having a distinct taste and/or flavor, such as a salt or any other taste or flavor potentiator or modifier. Examples of food additives include, but are not limited to, marinades and proteolytic enzymes. In addition, components that by themselves are not additives, such as vitamins, minerals, color additives, herbal additives (e.g., echinacea or St. John's Wort), antimicrobials, preservatives, and the like can be considered food additives.
- As used herein, the term "food product" refers to any nourishing substance that is eaten or otherwise taken into the body to sustain life, provide energy, promote growth, and/or the like. For example, in some embodiments, food products can include, but are not limited to, meats, vegetables, fruits, starches, and combinations thereof. In some embodiments, food products can include individual food components or mixtures thereof.
- As used herein, the term "heat seal" refers to any seal of a first region of a film surface to a second region of a film surface, wherein the seal is formed by heating the regions to at least their respective seal initiation temperatures. Heat-sealing is the process of joining two or more thermoplastic films or sheets by heating areas in contact with each other to the temperature at which fusion occurs, usually aided by pressure. In some embodiments, heat-sealing can be inclusive of thermal sealing, melt-bead sealing, impulse sealing, dielectric sealing, and/or ultrasonic sealing. The heating can be performed by any one or more of a wide variety of means, such as (but not limited to) a heated bar, hot wire, hot air, infrared radiation, ultrasonic sealing, and the like.
- As used herein, the term "lamination", the term "laminate", and the phrase "laminated film", can refer to the process and resulting product made by bonding together two or more layers of film and/or other materials. Lamination can be accomplished by joining film layers with adhesives, joining with heat and pressure, spread coating, and/or extrusion coating. In some embodiments, the term "laminate" can be inclusive of coextruded multilayer films comprising one or more tie layers.
- As used herein, the term "marinade" refers to an edible substance that can impart one or more flavors and/or textures to a food product. In some embodiments, the marinade can comprise acidic ingredients, such as vinegar, lemon juice, and/or wine. In some embodiments, the marinade can comprise savory ingredients, such as soy sauce, brine, or other prepared sauces. In some embodiments, the marinade can comprise oils, herbs, and spices to further flavor a food item. In some embodiments, the marinade can comprise one or more proteolytic enzymes to flavor the food and/or to tenderize a food product.
- As used herein, the term "meat" comprises both cooked and uncooked meat and includes, but is not limited to, beef, birds such as poultry (including chicken, duck, goose, turkey, and the like), buffalo, camel, crustacean (including shellfish, clams, scallops, mussels, oysters, lobster, crayfish, crab, shrimp, prawns, and the like), dog, fish (including salmon, trout, eel, cod, herring, plaice, whiting, halibut, turbot, ling, squid, tuna, sardines, swordfish, dogfish, shark, and the like), game (including deer, eland, antelope, and the like), game birds (such as pigeon, quail, doves, and the like), goat, hare, horse, kangaroo, lamb, marine mammals (including whales and the like), amphibians (including frogs and the like), monkey, pig, rabbit, reptiles (including turtles, snakes, alligators, and the like), and/or sheep.
- As used herein, the term "oriented" refers to a polymer-containing material that has been stretched at an elevated temperature (the orientation temperature), followed by being "set" in the stretched configuration by cooling the material while substantially retaining the stretched dimensions. Upon subsequently heating unrestrained, unannealed, oriented polymer-containing material to its orientation temperature, heat shrinkage is produced almost to the original unstretched, i.e., pre-oriented dimensions. More particularly, the term "oriented", as used herein, can refer to oriented films, wherein the orientation can be produced in one or more of a variety of manners.
- As used herein, the term "package" refers to packaging materials configured around a product being packaged, and can include (but are not limited to) bags, pouches, trays, and the like.
- As used herein, the term "polymer" refers to the product of a polymerization reaction, and can be inclusive of homopolymers, copolymers, terpolymers, etc. In some embodiments, the layers of a film can consist essentially of a single polymer, or can have still additional polymers together therewith, i.e., blended therewith.
- As used herein, the term "proteolytic enzyme" refers to an enzyme that can be added to a marinade fluid to sever peptide bonds in proteins, and therefore tenderize a meat. Proteolytic enzymes suitable for use with the presently disclosed subject matter can include, but are not limited to, bromelain from pineapple and papain from papaya, achromopeptidase, aminopeptidase, ancrod, angiotensin converting enzyme, bromelain, calpain, calpain I, calpain II, carboxypeptidase A, carboxypeptidase B, carboxypeptidase G, carboxypeptidase P, carboxypeptidase W, carboxypeptidase Y, caspase, caspase 1, caspase 2, caspase 3, caspase 4, caspase 5, caspase 6, caspase 7, caspase 8, caspase 9, caspase 10, caspase 11, caspase 12, caspase 13, cathepsin B, cathepsin C, cathepsin D, cathepsin G, cathepsin H, cathepsin L, chymopapain, chymase, chymotrypsin a-, clostripain, collagenase, complement Clr, complement Cls, complement Factor D, complement Factor I, cucumisin, dipeptidyl peptidase IV, elastase (leukocyte), elastase (pancreatic), endoproteinase Arg-C, endoproteinase Asp-N, endoproteinase Glu-C, endoproteinase Lys-C, enterokinase, factor Xa, ficin, furin, granzyme A, granzyme B, HIV protease, IGase, kallikrein tissue, leucine aminopeptidase (general), leucine aminopeptidase (cytosol), leucine aminopeptidase (microsomal), matrix metalloprotease methionine amiopeptidase, neutrase, papain, pepsin, plasmin, prolidase, pronase E, prostate specific antigen, protease (alkalophilic form), Streptomyces griseus, protease from Aspergillus, protease from Aspergillus saitoi, protease from Aspergillus sojae, protease (B. licheniformis) (Alkaline), protease (B. licheniformis) (Alcalase), protease from Bacillus polymyxa, protease from Bacillus sp, protease from Bacillus sp (Esperase), protease from Rhizopus sp., protease S, proteasomes, proteinase from Aspergillus oryzae, proteinase 3, proteinase A, proteinase K, protein C, pyroglutamate amiopeptidase, renin, rennin, streptokinase, subtilisin, thermolysin, thrombin, tissue plasminogen activator, trypsin, tryptase, urokinase, and combinations thereof.
- As used herein, the term "rupturable" with regard to a seal can indicate the susceptibility of being broken without implying weakness. Thus, in referring to a rupturable seal between the films of a package, it can be meant that when so sealed the films are united together in a fluid impervious manner, and when the seal is broken or severed by delamination of the films from one another in the area of the seal, the films are separated apart from one another severing the seal while still maintaining the integrity of the individual films themselves. Thus, the rupturable seal in an intact state serves to maintain the integrity of the product chamber reservoir for maintaining fluid, semi-fluid, and/or solid products therein but in a broken or severed state allows for passage of these products between the films along a delaminated seal area.
- As used herein, the term "seal" refers to any seal of a first region of an outer film surface to a second region of an outer film surface, including heat or any type of adhesive material, thermal or otherwise. In some embodiments, the seal can be formed by heating the regions to at least their respective seal initiation temperatures. The sealing can be performed by any one or more of a wide variety of means, including, but not limited to, using a heat seal technique (e.g., melt-bead sealing, thermal sealing, impulse sealing, dielectric sealing, radio frequency sealing, ultrasonic sealing, hot air, hot wire, infrared radiation, etc.).
- As used herein, the phrases "seal layer", "sealing layer", "heat seal layer", and "sealant layer", refer to an outer film layer, or layers, involved in the sealing of the film to itself, another film layer of the same or another film, and/or another article that is not a film. It should also be recognized that in general, up to the outer 3 mils of a film can be involved in the sealing of the film to itself or another layer. With respect to packages having only fin-type seals, as opposed to lap-type seals, the phrase "sealant layer" generally refers to the inside film layer of a package, as well as supporting layers adjacent this sealant layer often being sealed to itself, and frequently serving as a food contact layer in the packaging of foods. In general, a sealant layer sealed by heat-sealing layer comprises any thermoplastic polymer. In some embodiments, the heat-sealing layer can comprise, for example, thermoplastic polyolefin, thermoplastic polyamide, thermoplastic polyester, and thermoplastic polyvinyl chloride. In some embodiments, the heat-sealing layer can comprise thermoplastic polyolefin.
- As used herein, the phrase "thermoforming layer" refers to a film layer that can be heated and drawn into a cavity while maintaining uniform thinning, as opposed to films or film layers that lose integrity during the thermoforming process (e.g., polyethylene homopolymers do not undergo thermoforming with uniform thinning). In some embodiments, thermoforming layers can comprise, but are not limited to, polyamide, ethylene/propylene copolymer, and/or propylene homopolymer; in some embodiments, nylon 6, nylon 6/6, amorphous nylon, ethylene/propylene copolymer, and/or propylene homopolymer.
- As used herein, the term "thermoplastic" refers to uncrosslinked polymers of a thermally sensitive material that flow under the application of heat or pressure.
- As used herein, the term "tie layer" refers to any internal layer having the primary purpose of adhering two layers to one another. In some embodiments, tie layers can comprise any nonpolar polymer having a polar group grafted thereon, such that the polymer is capable of covalent bonding to polar polymers such as polyamide and ethylene/vinyl alcohol copolymer. In some embodiments, tie layers can comprise at least one member selected from the group including, but not limited to, modified polyolefin, modified ethylene/vinyl acetate copolymer, and/or homogeneous ethylene/alpha-olefin copolymer. In some embodiments, tie layers can comprise at least one member selected from the group consisting of anhydride modified grafted linear low density polyethylene, anhydride grafted low density polyethylene, homogeneous ethylene/alpha-olefin copolymer, and/or anhydride grafted ethylene/vinyl acetate copolymer.
- As used herein, terminology employing a "/" with respect to the chemical identity of a copolymer (e.g., "an ethylene/alpha-olefin copolymer"), identifies the comonomers that are copolymerized to produce the copolymer. Such phrases as "ethylene alpha-olefin copolymer" are the respective equivalent of "ethylene/alphaolefin copolymer."
-
Figure 1 illustrates apackage assembly 100 consistent with an exemplary embodiment of the present invention. Thepackage assembly 100 contains at least afirst package 200 and asecond package 300. Thefirst package 200 may contain two or more compartments. Afirst compartment 225 may substantially contain thesecond package 300 and asecond compartment 230 may substantially contain one ormore food products 110, such as a meat. Thesecond package 300 may contain one ormore food additives 120, such as a marinade. Although thesecond package 300 is substantially contained in thefirst compartment 225 of the first package, thesecond package 300 may include areputable seal 350a located proximate thesecond compartment 230. As explained in more detail further below, applying pressure to at least thefirst compartment 225 and, thus, thesecond package 300 may break the rupturable seal 310 to distribute thefood additive 120 from thesecond package 300 to thefood product 110 in thesecond compartment 230 of the first package. Thefirst package 200 may include a perimeterhard seal 235 configured to withstand the applied pressure and, thus, prevent the leaking of any of thefood product 110 or thefood additive 120 from the first package during the distribution of thefood additive 120. Thus, the presently disclosed subject matter achieves, among other things, controlled application of a food additive to a food product within apackage assembly 100. After sufficient marinating time, the marinated food product can be removed from package assembly and heated and/or cooked in an oven or microwave. -
Figure 2 illustrates an example of afirst package 200 without the second package, any food additives or food products. Thefirst package 200 can be fabricated from afirst film 215 that is extruded and thermoformed to produce thefirst compartment 225 and thesecond compartment 230. In the illustrated embodiment, the first and second compartments are separated from another by apartition 240 defined by two inner walls of thecompartments Figure 2 , one of ordinary skill in the art would recognize that the presently disclosed subject matter can include package configurations with more than two compartments. Asecond thermoplastic film 220 can be hermetically sealed to firstthermoplastic film 215 through aperimeter seal 235 such that the compartmentedfirst package 200 is substantially air and liquid tight. Theperimeter seal 235 extends around the perimeter offirst package 200 to create an airtight container. In some embodiments, e.g., the illustrated embodiment, thefirst film 215 and/or thesecond film 220 can be transparent so that the contents of the first package can be viewed. - The first package may be include a secondary seal (not illustrated) to provide additional strength to one or more compartments of the first package as further disclosed in
U.S. Patent Application Serial No. 12/079,409 filed on March 26, 2008 (entitled "On-Demand Meat Tenderizing Package"; Attorney Docket No. D-44119-01) and assigned to the assignee of the present application. - Referring back to the
perimeter seal 235, theperimeter seal 235 can be used to reliably contain thesecond package 300 containing the food additive and the food product in their respective compartments at normal operating pressures before, during, and after marinating. Theperimeter seal 235 can also provide a margin of safety to contain the contents of thefirst package 200 in the event that the first package is dropped, bumped, and/or otherwise transiently exposed to higher pressures either before therupturable seal 350 of the second package is broken or afterwards. - Moreover, the perimeter seal 235 (and/or, in embodiments having a secondary seal, the secondary seal) can be configured to be a hard or permanent seal in that the strength of the seal is intended to be strong enough to prevent rupture or the strength of the seal is intended to be equal to or higher than the strength of the sealed
plastic films -
Figures 1 and2 illustrate that thefirst package 200 can be closed on all four edges. In some embodiments, one or more of the edges can comprise sealed edges. For example, in embodiments in which the first package is formed from two separate sheets of plastic film, the four edges may all be sealed edges. Thus, thefirst package 200 may be formed byheat sealing films second compartments - In some embodiments, the heat sealing machine includes a heated seal bar that contacts and compresses the two films to be heat sealed together to form the
perimeter seal 235. Generally, three variables can be considered in forming a heat seal: the seal bar temperature, the dwell time, and the sealing pressure. The seal bar temperature can refer to the surface temperature of the seal bar. The dwell time can refer to the length of time that the heated seal bar contacts the film to transfer heat from the seal bar to soften at least a portion of the films (e.g., the sealing layers of the films) so that they can be melded together. The sealing pressure can refer to the amount of force that squeezes the films together during this heat transfer. All of these variables can be modified accordingly in order to prepare a package suitable with the presently disclosed subject matter. - Because the heat sealing layers for much of the thermoplastic packaging films used in food packaging are based on relatively low-melting polyolefin thermoplastics (or similar melt-temperature thermoplastics), the heat sealing machines present in food packaging plants can be designed and set to operate with a seal bar temperature, a dwell time, and a sealing pressure in a range useful for such materials to permit the heat sealing machines to operate at high speeds to form strong seals.
- Although the films of presently disclosed
package 200 may be heat-sealed to formperimeter seal 235, the use of other adhesives or mechanical closures (e.g., clips) as desired or necessary is within the scope of the presently disclosed subject matter. Particularly, adhesives can be applied in a desired pattern, or sealed at a certain temperature (such as with a layer of ionomer) to define seal strength in a directly proportional fashion; i.e., more adhesive or higher temperature can create a stronger seal, while less adhesive or lower temperature can produce a weaker seal. - In some embodiments, the
perimeter seal 235 may not be sealed until after thefirst package 200 is filled. For example, thefirst film 215 is formed into a compartmented support member having at least two compartments adapted to contain a second package and a food product. The compartmented support member is then loaded with a second package containing the food additive and the food product. Thesecond film 220 can be positioned to contact thefirst film 215 at least along the perimeter of the first package. A vacuum can then be applied to the compartments. Thesecond film 220 can then be sealed around the perimeter of the compartmented support member to form theperimeter seal 235 in this regard thesecond film 220 can function as a cover to the support member. -
Figure 3 illustrates an example of asecond package 300 without any food additives. Thesecond package 300 can be fabricated similar to thefirst package 200 as described in the above exemplary embodiment in that two films may be sealed together along four edges to form a package. Alternatively, the second package can include a first film that is folded unto itself such that the fold in the first film forms an edge of the package and the remaining edges may be sealed together. In the illustrated embodiment, thesecond package 300 can be fabricated from thefirst film 315 that is extruded and thermoformed to produce acompartment 325 and afirst part 350 of a flange extending away from thecompartment 325. Thesecond film 320 can be hermetically sealed to firstthermoplastic film 315 through aperimeter seal 335 such that thecompartment 325 is substantially air and liquid tight. Theperimeter seal 335 extends substantially around the perimeter of thesecond package 300 to create an airtight container. Thesecond film 320 may also define asecond part 355 of the flange that corresponds to thefirst part 350. Theperimeter seal 335 or another seal may be used to seal the first andsecond parts flange 360 of the second package. In some embodiments, e.g., the illustrated embodiment, thefirst film 315 and thesecond film 320 can be transparent so that the contents of thesecond package 300 can be viewed. Thesecond package 300 or, more particularly, thecompartment 325 of thesecond package 300 may be configured to substantially fit into and, thus, be contained in thefirst compartment 225 offirst package 200. Therefore, thesecond package 300 can be adapted to be slightly smaller than the first compartment of thefirst package 200. -
Figures 1 and3 illustrate that thesecond package 300 can be closed on all four edges. In some embodiments, one or more of the edges can comprise sealed edges. For example, in embodiments in which the second package is formed from two separate sheets of plastic film, the four edges may all be sealed edges. Thus, thesecond package 300 can be formed by heat sealing the twofilms - In some embodiments, the heat sealing machine includes a heated seal bar that contacts and compresses the two films to be heat sealed together to form the
perimeter seal 335. Generally, three variables can be considered in forming a heat seal: the seal bar temperature, the dwell time, and the sealing pressure. The seal bar temperature can refer to the surface temperature of the seal bar. The dwell time can refer to the length of time that the heated seal bar contacts the film to transfer heat from the seal bar to soften at least a portion of the films (e.g., the sealing layers of the films) so that they can be melded together. The sealing pressure can refer to the amount of force that squeezes the films together during this heat transfer. All of these variables can be modified accordingly in order to prepare a package suitable with the presently disclosed subject matter. - Because the heat sealing layers for much of the thermoplastic packaging films used in food packaging are based on relatively low-melting polyolefin thermoplastics (or similar melt-temperature thermoplastics), the heat sealing machines present in food packaging plants can be designed and set to operate with a seal bar temperature, a dwell time, and a sealing pressure in a range useful for such materials to permit the heat sealing machines to operate at high speeds to form strong seals.
- Although the films of the
second package 300 may be heat-sealed to form theperimeter seal 335, the use of other adhesives or mechanical closures (e.g., clips) as desired or necessary is within the scope of the presently disclosed subject matter. Particularly, adhesives can be applied in a desired pattern, or sealed at a certain temperature (such as with a layer of ionomer) to define seal strength in a directly proportional fashion; i.e., more adhesive or higher temperature can create a stronger seal, while less adhesive or lower temperature can produce a weaker seal. - In some embodiments, the
perimeter seal 335 may not be sealed until after thesecond package 300 is filled. For example, thefirst film 315 can be formed into a support member having acompartment 325 adapted to contain a food additive and a defining afirst part 350 of a flange. Thecompartment 325 may then be loaded with a food additive. Next, thesecond film 320 can be positioned to contact thefirst film 315, at least, along the perimeter of the second package. A vacuum can then be applied to thecompartment 325. Thesecond film 320 can then be sealed around the perimeter of the support member to formperimeter seal 335. In this regard, thesecond film 320 can function as a cover that is sealed to the support member. - The filling of the food additive into the second package and the sealing of the second package may incur before or after the second package is placed into the first compartment of the first package. For example, the filing and sealing operations of the second package may incur before the introduction of the first package. Indeed, the filing and sealing operations may incur at a different location or even facility than the forming and sealing of the first package. Such an embodiment may reduce the likelihood of cross-contamination of the food additive and the food product.
- Referring back to the
perimeter seal 335 of the second package, theperimeter seal 335 or one or more portions thereof may be designed to break when exposed to a predetermined pressure, referred to as being rupturable. In general, therupturable perimeter seal 335 of the second package is particularly configured to have a lower rupture pressure compared to perimeter hard seal 235 (and, in embodiments having a secondary seal, the secondary seal) of the first package such that the seal(s) of the first package is unaffected by the rupture of perimeterrupturable seal 335 of the second package. In addition, perimeterrupturable seal 335 may be configured to rupture in a controlled manner across a sufficient area to provide a relatively low-pressure movement of a flowable food additive (such as marinade) out of thecompartment 325 of the second package. - Although the entire perimeter seal of the second package may be configured to rupture, in other embodiments, the perimeter seal may have only a portion that is configured to rupture, e.g., the portion extending across the flange or, more specifically, the second package may include a first permanent seal that extends around the perimeter except for the portion extending across the flange and a second rupturable seal that extends across the flange. In such an embodiment, when pressure is applied, the second rupturable seal is intended to rupture before the first permanent seal and, thus, the food additives would escape through the flange only.
- A rupturable seal can be formed by any of a number of various techniques known in the art. Particularly, it will be understood that there are a number of ways of making a rupturable seal in accordance with the presently disclosed subject matter, including, but not limited to, one or more of zone patterning, adhesive, ultrasonic welding, thermal bonding, crimping, cohesives, compression, nipping, needle punching, sewing, hydroentangling, and the like. For example, in some embodiments, rupturable seal can be formed of a pattern of printed ink that prevents the package films from heat sealing at an inked portion, such that the amount of inked portions in the ink pattern determine the strength of the seal. In some embodiments, rupturable seal can be fabricated by means of a discontinuity within the seal width. For example, one discontinuity within rupturable seal can include one or more stress concentrators having an inflection point that is more responsive to the interior bag pressure force than other portions that are relatively straight or smoothly curved.
- Continuing, in some embodiments, a rupturable seal can be comprised of incompatible polymer blends. For example, each of the
films films films - In some embodiments, the strength of a rupturable seal can be manipulated by the temperature, dwell time and/or pressure of the heat seal bar, depending on the type and thickness of the sealant being applied. It is to be understood that the pressure required to a separate rupturable seal can depend upon the width of the sealed area at the inner end thereof. Thus, the size and configuration of rupturable seal can be altered to vary the pressure within the sealed enclosure required to rupture the seal.
- Referring back to
Figure 1 and referring toFigure 4 , thesecond package 300 is substantially contained in thefirst compartment 225 of thefirst package 200. Theflange 360 of the second package extends from thefirst compartment 225 of the first package toward thesecond compartment 230 of the first package. More specifically, theflange 360 extends from thefirst compartment 225 at least partially across thepartition 240 separating the first andsecond compartments second compartment 230 such that thesecond package 300 is in fluid communication with thesecond compartment 230 when the rupturable seal 335a across theflange 360 ruptures. For example, when pressure is applied to thesecond package 300 and the rupturable seal 335a across theflange 360 ruptures, thefood additive 120 in thesecond package 300 may leave thesecond package 300 via theflange 360 into thesecond compartment 230 and interact with thefood product 120 contained in thesecond compartment 230. Even as pressure is applied to thesecond package 300 through thefirst package 200, the perimeterhard seal 235 of the first package is configured to prevent any of thefood additive 120 orfood product 110 from leaking out of thefirst package 200. - As discussed above, one or more of the first package and the second package can be manufactured through an extrusion molding and thermoform molding process. As a more specific example, the
first package 200 can be fabricated from thefirst film 215 that is extruded and thermoformed to produce thefirst compartment 225 and thesecond compartment 230. Extrusion molding is well known plastic shaping processing in which, e.g., thermoplastic material are fed from a hopper or other device into an extruder configured to heat the thermoplastic material and force it through a die to form and particular profile such as a plastic film or sheet. Thermoforming is well known in the packaging art, and is the process whereby a thermoplastic web is heat softened and reshaped to conform to the shape of a cavity in a mold. Suitable thermoforming methods, for example, include a vacuum forming or plug-assist vacuum forming method. In a vacuum forming method, the first web is heated, for example, by a contact heater, and a vacuum is applied beneath the web causing the web to be pushed by atmospheric pressure down into a preformed mold. In a plug-assist vacuum forming method, after the first or forming web has been heated and sealed across a mold cavity, a plug shape similar to the mold shape impinges on the forming web and, upon the application of vacuum, the forming web transfers to the mold surface. - It should be noted herein that the
first film 215 of the first package may be considered a "bottom" web, e.g., in normal usage, the first package can rest on thefirst film 215 such that the web comprises the bottom offirst package 200. Likewise, thesecond film 200 may be considered a "top" web, e.g., in normal usage, the first package can be positioned such that the web of the second film comprises the top of the first package that covers the bottom web. This description is for convenience in understanding the presently disclosed subject matter. Nevertheless, those skilled in the art will understand, after a review of the presently disclosed subject matter, that the first package may be manufactured, stored, shipped, and/or displayed in any suitable orientation. For example, the first package may be placed on a supporting surface such that the thermoformed web functions as the top of the package and the covering web functions as the bottom of the package. - In some embodiments, the first and
second films U.S. Patent No. 6,769,227 to Mumpower , the content of which is incorporated herein in its entirety by reference thereto. Accordingly, films of the presently disclosed subject matter can be made by any suitable process, including coextrusion, lamination, extrusion coating, and combinations thereof. - The films used to form the disclosed packages can be provided in sheet or film form and can be any of the films commonly used for this type of packaging. In some embodiments, however, the film can be a commercially available multilayer film having a sealant layer, a barrier layer, and one or more abuse layers.
- Thus, in some embodiments, the first and second films of the first package may comprise one or more barrier layers. Such barrier layers can include, but are not limited to, ethylene/vinyl alcohol copolymer, polyvinylidene chloride, polyalkylene carbonate, polyamide, polyethylene naphthalate, polyester, polyacrylonitrile, and combinations thereof, as known to those of skill in the art. In some embodiments, the barrier layer can comprise either EVOH or polyvinylidene chloride, and the PVDC can comprise a thermal stabilizer (i.e., a HCl scavenger, such as epoxidized soybean oil) and/or a lubricating and/or processing aid, which are well known in the art.
- In some embodiments, the first and second films of the first package may comprise one or more seal layers. Such seal layers can include, but are not limited to, the genus of thermoplastic polymers, including thermoplastic polyolefin, polyamide, polyester, polyvinyl chloride, homogeneous ethylene/alpha-olefin copolymer, ethylene/vinyl acetate copolymer, ionomer, and combinations thereof.
- In some embodiments, the first and second films of the first package may comprise one or more tie layers. In some embodiments, tie layers can comprise any nonpolar polymer having a polar group grafted thereon, so that the polymer is capable of covalent bonding to polar polymers, such as polyamide and ethylene/vinyl alcohol copolymer. In some embodiments, tie layers can comprise at least one member of the group including, but not limited to, modified polyolefin, modified ethylene/vinyl acetate copolymer, homogeneous ethylene/alpha-olefin copolymer, and combinations thereof. In some embodiments, tie layers can comprise at least one member selected from the group including, but not limited to, anhydride modified grafted linear low density polyethylene, anhydride grafted low density polyethylene, homogeneous ethylene/alpha-olefin copolymer, and/or anhydride grafted ethylene/vinyl acetate copolymer.
- In some embodiments, the first and second films of the first package may comprise one or more abuse layers. In some embodiments, abuse layers can comprise any polymer, so long as the polymer contributes to achieving an integrity goal and/or an appearance goal. In some embodiments, the abuse layer can include, but is not limited to, polyamide, ethylene/propylene copolymer, nylon 6, nylon 6/6, amorphous nylon, and combinations thereof.
- In some embodiments, the first and second films of the first package may comprise one or more bulk layers to increase the abuse-resistance, toughness, modulus, etc., of the film. In some embodiments, the bulk layer can comprise polyolefin, including but not limited to, at least one member selected from the group consisting of ethylene/alphaolefin copolymer, ethylene/alpha-olefin copolymer plastomer, low density polyethylene, and linear low density polyethylene.
- The polymer components used to fabricate the films according to the presently disclosed subject matter can also comprise appropriate amounts of other additives normally included in such compositions. For example, slip agents (such as talc), antioxidants, fillers, dyes, pigments and dyes, radiation stabilizers, antistatic agents, elastomers, and the like can be added to the disclosed films.
- Generally, the films employed in the presently disclosed subject matter can be multilayer or monolayer, although, of course, those films defined as delaminatable, multilayer films must include at least two layers. Typically, the films employed will have two or more layers in order to incorporate a variety of properties, such as, for example, sealability, gas impermeability and toughness, into a single film.
- In some embodiments, at least a portion of at least one film of the presently disclosed subject matter can be irradiated to induce cross-linking. In the irradiation process, the film is subjected to one or more energetic radiation treatments, such as corona discharge, plasma, flame, ultraviolet, X-ray, gamma ray, beta ray, and high energy electron treatment, each of which induces cross-linking between molecules of the irradiated material. The irradiation of polymeric films is disclosed in
U.S. Patent No. 4,064,296, to Bornstein et al. . - Films of the presently disclosed subject matter can have any total thickness desired, so long as the films provide the desired properties for the particular packaging operation in which the film is used. Final web thicknesses can vary, depending on process, end use application, and the like. Typical thicknesses range between 0.0025 to 0.51 mm (0.1 to 20 mils), in some embodiments between 0.0076 and 0.38 mm (0.3 and 15 mils), in some embodiments 0.013 to 0.25 mm (0.5 to 10 mils), in some embodiments 0.025 to 0.20 mm (1 to 8 mils), in some embodiments 0.076 to 0.15 mm (3 to 6 mils), such as 0.10 to 0.13 mm (4 to 5 mils). In some embodiments, top webs can have a thickness of between 0.05 and 0.13 mm (2 and 5 mils), and bottom webs can have a thickness of between 0.13 and 0.25 mm (5 and 10 mils).
- In some embodiments, the film according to the presently disclosed subject matter comprises a total of from about 4 to about 20 layers; in some embodiments, from about 4 to about 12 layers; and in some embodiments, from about 5 to about 9 layers. Thus, in some embodiments, the disclosed film can comprise 1, 2, 3, 4, 5, 6, 7, 8, 9, 10, 11, 12, 13, 14, 15, 16, 17, 18, 19, or 20 layers. Accordingly, the film of the disclosed package can have any total thickness desired, so long as the film provides the desired properties for the particular packaging operation in which the film is used, e.g. optics, modulus, seal strength, and the like.
- In some embodiments, first and second films of the first package may be transparent (at least in the non-printed regions) so that the packaged articles are visible through the films. "Transparent" as used herein means that the material transmits incident light with negligible scattering and little absorption, enabling objects (e.g., packaged food or print) to be seen clearly through the material under typical unaided viewing conditions (i.e., the expected use conditions of the material). The transparency (i.e., clarity) of the film can be at least about any of the following values: 20%, 25%, 30%, 40%, 50%, 65%, 70%, 75%, 80%, 85%, and 95%, as measured in accordance with ASTM D1746.
- Although the forgoing description regarding the films being described as the bottom and top webs, the manufacturing of the films, the different layers within the film including, but not limited to, barrier layers, tie layers, abuse layers, and bulk layers, and the schematic of Figure 7 as being applicable to the first package and its films, it will be evident to one skilled in the art that the foregoing description is equally applicable to the second package and its films.
- With respect to the seals of the first and second packages, in some embodiments, the seals can be formed using a heat sealing machine that includes a heated seal bar that contacts and compresses films together to form a seal. In particular and as an example, regarding the perimeter
hard seal 235 of the first package, after compression for a desired amount of time, the heating bar can then be removed to allow the sealed area to cool and form a sealed bond. The resultingperimeter seal 235 can extend continuously around the outside edge ofpackage 200 to hermetically seal or enclose the food product and/or the second package and thus food additive housed therein. In this manner, first andsecond films - The resulting
perimeter seal 235 between first andsecond films perimeter seal 235 can be at least about any of the following values: 7.0, 8.0, 9.0, and 10 pounds/inch or greater. The term "heat seal bond strength" as used herein can refer to the amount of force required to separate thesecond film 220 fromfirst film 215, as measured in accordance with ASTM F88-94 where the Instron tensile tester crosshead speed is 5 inches per second, using five, 1-inch wide representative samples. As discussed above, the strength of the perimeter seal may be equal to or greater than the strength of the films themselves or otherwise be considered permanent or a hard seal. - The rupturable seal 335a of the second package may be formed by any of a number of various techniques. Particularly, it will be understood that the rupturable seal 335a can be made using one or more of incompatible materials, zone patterning, adhesive, ultrasonic welding, thermal bonding, crimping, cohesives, compression, nipping, needle punching, sewing, hydro-entangling, and the like. A combination of these methods can also be used. In general the rupturable seal 335a of the second package is configured to have a lower strength than the
perimeter seal 235 of the first package and of any of the films of the second package. As an example, the strength of the rupturable seal 335a can be any of the following values 1.0, 2.0, 3.0. 4.0, 5.0, 6.0, 7.0, and 8.0 pounds/inch. - Referring back to the thermoforming processes, the processes may include a horizontal form, fill and seal machine, e.g., as partially shown in
Figures 5a ,5b and6 .Figure 5a illustrates adie box 500 for forming the compartmented support member of the first package. In particular thedie box 500 includes afirst cavity 510 for forming the first compartment andsecond cavity 520 for forming the second compartment. A sheet of film may be placed against the die box and the first and second compartments may be formed through a thermoforming process in which portions of the sheet of film are forced (through a plug and/or vacuum force) to assume the shape of the two cavities. Thesame die box 500 can be modified to form one or more second packages according to the exemplary embodiments described herein. For example, inserts may be used to modify the cavities to form compartments of the second packages rather than the first and second compartments of the first package. More specifically and as illustrated inFigure 5b , afirst insert 610 may be placed into thefirst cavity 510 such that thefirst insert 610 defines a modifiedfirst cavity 615 of the die box having a size slightly smaller than the unmodifiedfirst cavity 510. The intent of modifying the first cavity is to form a compartment of the second package that is slightly smaller than the first compartment of the first package and, thus, allow the compartment of the second package to fit into the first compartment. Asecond insert 620 may be placed into thesecond cavity 520. Thesecond insert 620 defines two cavities, referred to as asecond cavity 625 and athird cavity 630. Each of thesecond cavity 625 andthird cavity 630 is substantially the same as the modifiedfirst cavity 615 such that each of the second cavity and the third cavity form substantially the same size compartment as the modified first cavity. With the placement of theinserts die box 500 and three compartments may be formed through an extrusion process in which portions of the sheet of film are forced (through a plug and/or vacuum force) to assume the shape of the cavities. Once the compartments are formed, the food additives may be added to each of the compartments, a second sheet of film may be placed onto and sealed with the first sheet of film and compartments. A vacuum process may also be used to evacuate the atmosphere in the compartments prior to sealing the films together. Next, the first and second sealed films may be trimmed or cut to form three packages containing a food additive. The cutting operations may be used to define a flange of each package. As explained herein, the flange can be used as conduit between the first and second compartments of the first package.Figure 6 illustrates thesecond package 300 placed in afirst compartment 225 of a formedsupport member 215 of the first package. As illustrated, aflange 360 of the second package extends at least partially across thepartition 240 separating the first andsecond compartments Figure 6 ) may be placed into the second compartment. After the second package and the food products are loaded into the first and second compartments respectively, a second sheet of film or a cover may be placed onto and sealed with the support member and its compartments. A vacuum process may also be used to evacuate the atmosphere in the compartments prior to sealing them. Next, if necessary, the second sealed film or cover may be trimmed or cut to correspond to the bottom support member of the first package. - In addition to the hard seal along the perimeter of the first package, a second seal and a third seal may be applied to the first package. For example, along the partition, a second seal may be applied between the first plastic film of the first package and the first plastic film of the second package that corresponds to the flange of the second package. Similarly, along the partition, a third seal may be applied between the second plastic film of the second package and the second plastic film of the second package that corresponds to the flange of the second package. The second and third seals can be either a hard seal or rupturable seal. The intent of the second and third seals is to prevent the food product from leaking from the second compartment to the first compartment prior to the rupturing of the rupturable seal of the second package.
- As set forth in detail herein above, in some embodiments the
second compartment 230 of thefirst package 200 may comprise a food product, such as a cut of meat. Examples of meat that are suitable for use with the presently disclosed subject matter can include, but are not limited to, beef, birds such as poultry (including chicken, duck, goose, turkey, and the like), buffalo, camel, crustacean (including shellfish, clams, scallops, mussels, oysters, lobster, crayfish, crab, shrimp, prawns, and the like), dog, fish (including salmon, trout, eel, cod, herring, plaice, whiting, halibut, turbot, ling, squid, tuna, sardines, swordfish, dogfish, shark, and the like), game (including deer, eland, antelope, and the like), game birds (such as pigeon, quail, doves, and the like), goat, hare, horse, kangaroo, lamb, marine mammals (including whales and the like), amphibians (including frogs and the like), monkey, pig, rabbit, reptiles (including turtles, snakes, alligators, and the like), and/or sheep. In some embodiments, the food product can be whole, diced, minced, shaved, cut into strips, and/or formed into meatballs. - In some embodiments, meat substitutes can be used and are included under the term "meat". Such meat substitutes can approximate the aesthetic qualities and/or chemical characteristics of certain types of meat. The meat substitutes can include, but are not limited to, seitan, rice, mushrooms, legumes, tempeh, textured vegetable protein, soy concentrate, mycoprotein-based Quorn, modified defatted peanut flour, and/or pressed tofu to make the meat substitute look and/or taste like chicken, beef, lamb, ham, sausage, seafood, and the like.
- In some embodiments, the food product can comprise one or more vegetables. Vegetables that are particularly suited for use with the presently disclosed subject matter can include, but are not limited to, artichokes, asparagus, beans, bean sprouts, beets, broccoli, cauliflower, cabbage, carrots, celery, corn, collards, eggplant, green peppers, kale, leeks, mushrooms, mustard greens, onions, peas, potatoes, radishes, red peppers, rhubarb, spinach, squash, sweet potatoes, turnips, water chestnuts, watercress, yarns, yellow peppers, and/or zucchini. In some embodiments, the vegetable can be diced, minced, shaved, and/or cut into strips.
- Accordingly, the food product suitable for use with the presently disclosed subject matter is not particularly limited. The presently disclosed methods and package can be applied to raw (i.e., uncooked) food products, partially cooked food products, and/or pre-cooked products, where the cooking process is intended to cook, completely cook, and/or re-heat the food product. Thus, the food product selected can be any type that is suitable for consumption. The food product can be non-rendered, non-dried, raw, and can comprise mixtures of whole muscle meat formulations. Whole meat pieces can be fresh, although frozen or semi-frozen forms can also be used. Since freezing affects the tenderness of meat by rupturing intrafibrillar tissue as a result of ice crystal formation, the increased tenderness resulting from freezing can be taken into account when using such products in the package and methods described herein.
- As set forth in detail herein above, in some embodiments, the
first compartment 225 of thefirst package 200 can substantially contain asecond package 300 which may house a food additive, such as marinade. The amount of marinade to be used in the presently disclosed subject matter depends on the type and added amount of food additive. The food additive can be in any form including, but not limited to, liquid, paste, powder, and/or combinations thereof. In some embodiments, the food additive can be in the form of liquid or powder from the standpoint of handleability, preservability, and the like. If the food additive of the presently disclosed subject matter is used in liquid form, it can be in the form of solution or dispersion in water or an aqueous liquid or in the form of solution or dispersion in fatty oil. In some embodiments, the food additive can be frozen when added to package in order to allow heat sealing mechanisms to function appropriately. That is, when a liquid food additive is added to package, the liquid nature of the food additive can interfere with the heat sealing process, producing a non-hermetic seal. - In some embodiments, the food additive can comprise one or more enzymatic tenderizers to form a tenderized meat product. Particularly, one or more proteolytic enzymes can be added to the food additive to sever peptide bonds in proteins, and therefore tenderize the meat. Proteolytic enzymes suitable for use with the presently disclosed subject matter can include, but are not limited to, bromelain from pineapple and papain from papaya, achromopeptidase, aminopeptidase, ancrod, angiotensin converting enzyme, bromelain, calpain, calpain I, calpain II, carboxypeptidase A, carboxypeptidase B, carboxypeptidase G, carboxypeptidase P, carboxypeptidase W, carboxypeptidase Y, caspase, caspase 1, caspase 2, caspase 3, caspase 4, caspase 5, caspase 6, caspase 7, caspase 8, caspase 9, caspase 10, caspase 11, caspase 12, caspase 13, cathepsin B, cathepsin C, cathepsin D, cathepsin G, cathepsin H, cathepsin L, chymopapain, chymase, chymotrypsin a-, clostripain, collagenase, complement Clr, complement Cls, complement Factor D, complement Factor I, cucumisin, dipeptidyl peptidase IV, elastase (leukocyte), elastase (pancreatic), endoproteinase Arg-C, endoproteinase Asp-N, endoproteinase Glu-C, endoproteinase Lys-C, enterokinase, factor Xa, ficin, furin, granzyme A, granzyme B, HIV protease, IGase, kallikrein tissue, leucine aminopeptidase (general), leucine aminopeptidase (cytosol), leucine aminopeptidase (microsomal), matrix metalloprotease, methionine amiopeptidase, neutrase, papain, pepsin, plasmin, prolidase, pronase E, prostate specific antigen, protease (alkalophilic form), Streptomyces griseus, protease from Aspergillus, protease from Aspergillus saitoi, protease from Aspergillus sojae, protease (B. licheniformis) (Alkaline), protease (B. licheniformis) (Alcalase), protease from Bacillus polymyxa, protease from Bacillus sp, protease from Bacillus sp (Esperase), protease from Rhizopus sp., protease S, proteasomes, proteinase from Aspergillus oryzae, proteinase 3, proteinase A, proteinase K, protein C, pyroglutamate amiopeptidase, renin, rennin, streptokinase, subtilisin, thermolysin, thrombin, tissue plasminogen activator, trypsin, tryptase, urokinase, and combinations thereof.
- In some embodiments, the food additive can comprise additional components, including but not limited to, bactericides, fungicides or other preservatives, wetting agents (e.g., a Tween), antioxidants, viscosity control agents (e.g., gums), brine (e.g., sodium chloride, phosphates, dextrose), curing agents (e.g., nitrites, sugars, erythorbate), flavoring agents (e.g., herbs, spices, and liquid smoke), and the like.
- As set forth in detail hereinabove, the
second package 300 can be prepared such that thefirst film 315 of the second package can be formed into acompartment 325. A food additive 120 (e.g., a marinade) can be placed in thecompartment 325. Thesecond film 320 can hermetically seal thefood additive 120 within thesecond package 300. - The
first package 200 can be prepared such thatfirst film 215 of the first package can be formed into first andsecond compartments second compartment 230. Thesecond package 300 containing thefood additive 120 can be placed in thefirst compartment 230. Alternatively, thesecond package 300 can first be placed into thefirst compartment 225 of the first package and then thefood additive 120 can be placed into thesecond package 300. Thesecond film 220 of the first package can hermetically seal thefood product 110 and thesecond package 300 and, thus, thefood additive 120 within thesecond package 300. - Thus, in some embodiments, the presently disclosed subject matter is directed to a
package assembly 100 for marinating and/or heating a food product. Thepackage assembly 100 includes afirst package 200 and asecond package 300 contained within thefirst package 200. In some embodiments, each of the first andsecond package thermoformed film first package 200 may have afirst compartment 225 and asecond compartment 230 and thesecond package 300 may have a compartment 325) and asecond thermoplastic film thermoformed film food additive 120 can be disposed in thecompartment 325 of the second package and thesecond package 300 can be disposed in thefirst compartment 225 of the first package. Afood product 110 can be disposed in thesecond compartment 230 of the second package. The first andsecond films perimeter seal 235 around the perimeter of thefirst package 200. Theperimeter seal 235 of the first package may be a hard seal in that the seal is not intended to rupture (e.g., the strength of the seal may be at least equal to the strength of the first and second films.). The first andsecond films perimeter seal 335 around the perimeter of thesecond package 300. At least a portion 335a of the perimeter seal of the second package, e.g., the portion extending across aflange 360 of the second package, can be a rupturable seal. The rupturable seal 335a is configured to rupture in response to applied pressure, e.g., the strength of the seal 335a may be less than that of any of thefilms perimeter seal 235 of the first package. Theflange 360 of the second package can extend from thefirst compartment 225 of the first package at least partially over apartition 240 between the first andsecond compartments second compartment 230 of the first package such that thesecond package 300 is in fluid communication with thesecond compartment 230 of the first package when the rupturable seal 335a ruptures. - At a desired time, a user can grip the
package assembly 100, and using his or her thumbs or a hard object, emit pressure on thefirst compartment 225 of the first package and thus onto thesecond package 300 contained substantially therein. Upon the increased pressure, the rupturable seal 335a of the second package will fail, allowing thefood additive 120 contained in thesecond package 300 to flow from thecompartment 325 of the second package through theflange 360 of the second package and into thesecond compartment 230 of the first package to freely mix with thefood product 110 stored in thesecond compartment 230 of the first package. Theperimeter seal 235 of the first package is configured to be strong enough to minimize the likelihood that theperimeter seal 235 would rupture or otherwise leak during this process and thus thefood additive 120 and thefood product 110 are contained within thefirst package 200 even when the pressure is applied for the user. In order to facilitate mixing, the user can shake or rotate thepackage assembly 100 to fully mix thefood product 110 and thefood additive 120. - The
package assembly 100 can then be marinated for a desired amount of time. In some embodiments, thepackage assembly 100 can be incubated a sufficient time to allow the food product to tenderize to a desired amount. Thus, in some embodiments, the presently disclosed subject matter is directed to a method of controlling the level of food additive imparted to a food product. The method may comprise forming a second package including thermoforming a first thermoplastic film of the second package into a compartmented support member having a compartment; forming a first package including thermoforming a first thermoplastic film of the first package a compartmented support member having at least two compartments; loading the compartment of the second package with a food additive; applying a vacuum to the compartment of the second package; sealing the compartment with a second thermoplastic film of the second package and defining a flange of the second package, wherein the sealing includes providing a rupturable seal across the flange; loading the second package into the first compartment of the first package such that the flange of the second package extends at least partially over a partition between the first and second compartments of the first package; loading a food product in the second compartment of the first package; applying a vacuum to at least the second compartment of the first package; and sealing the first and second compartments of the first package with a second thermoplastic film of the first package, wherein the sealing includes providing a hard seal around the perimeter of the first package. - In addition to the advantages that would be evident to one skilled in the art regarding the presently disclosed subject matter, the use of a second package to contain the food additive may have one or more additional advantages. For example, rather than loading the food additive directly into the first compartment of the first package around the same time as the loading of the food product directly into the second compartment of the first package, the loading of the food additive into a second package first may minimize the likelihood of any premature cross-contamination between the food additive and the food product. Moreover, loading the food additive and the food product directly into compartments at the same time may require that the food additive be frozen to allow the machinery to advance rapidly as well as to prevent flashing of a liquid as the vacuum is applied to the food product. Freezing the food additive may be costly and require time and the maintenance of an environment below 0°F. The thawing of the food additive after the packaging operations may create condensation on the surface of the package which may create aesthetic issues and may transfer to any cardboard boxing packaging used in connection with the package and weaken the cardboard. In the presently disclosed subject matter, in some embodiments, the food additive may be handled as a liquid which may allow for more options for handling and flashing of the liquid may be eliminated because less vacuum may be needed to pull the surface air from the package. Also, using a liquid would eliminate the limitations of a frozen food additive as discussed above.
- Also, the use of a second package for the food additive, allows for the first package to be specifically configured to hold the food product and the second package to be specifically configured to hold the food additive. For example, the materials of the first package can be "breathable" which may be preferred for food products such as fish or chicken and the materials of the second package may include barrier layers which may be preferred for the food additive. The second packages may be labeled or printed individually and then placed in a first package so a customer may change from one type to another type of food additive without changing the top web of film used for the first package even if it is printed for a particular food product.
- The use of the second package also allows for the seals to be specifically configured for particular functions. For example and as discussed above, the perimeter seal of the first package may be a hard seal that reduces the likelihood of the first package rupturing or otherwise leaking even as the user applies pressure or shakes the package assembly to mix the food additive and food product, while the rupturable seal of the second package is specifically configured to rupture and allow the food additive and the food product to mix.
- Many modifications and other embodiments of the inventions set forth herein will come to mind to one skilled in the art to which these inventions pertain having the benefit of the teachings presented in the foregoing descriptions and the associated drawings whereby the scope of the invention is defined by the appended claims.
Claims (15)
- A package assembly (100) for marinating a food product comprising:a first package (200) comprising a first compartment (225) that substantially contains a second package (300) and a second compartment (230) configured to contain a food product (110); whereinthe second package (300) is configured to contain a food additive (120) and includes a rupturable seal (335a) configured to rupture and allow the food additive to escape the second package (300) when exposed to a rupture pressure, wherein the second package (300) is in fluid communication with the second compartment (230) upon a rupturing of the rupturable seal (335a) so as to allow the food additive to mix with the food product (110), andwherein the first package (200) is configured to withstand the rupture pressure and prevent leaking of the food additive (120) and food product (110) from the first package (200) during the mixing of the food additive (120) and the food product (110).
- The package assembly according to Claim 1, wherein the first package (200) includes a first plastic film (215) of the first package (200) and a second plastic film (220) of the first package (200) sealed together by a hard seal (235) configured to withstand the rupture pressure.
- The package assembly of Claim 2, wherein the first plastic film (215) is a thermoformed film formed into a compartmented support member having the first and second compartments (225, 230).
- The package assembly according to Claim 2, wherein the second package (300) includes a first plastic film (315) of the second package (300) and a second plastic film (320) of the second package (300) sealed together at least partially by the rupturable seal (335a).
- The package assembly according to Claim 4, wherein the first plastic film (315) of the second package (300) and the second plastic film (320) of the second package (300) collectively form a flange (360) of the second package (300) and the rupturable seal (335a) extends at least across the flange (360) of the second package (300).
- The package assembly according to Claim 5, wherein the rupturable seal (335a) extends around the perimeter of the first plastic film (315) of the second package (300) and the perimeter of the second plastic film (320) of the second package (300).
- The package assembly according to Claim 6, wherein the first and second compartments (225, 230) of the first package (200) are separated by a partition (240) and the flange (360) of the second package (300) extends from the first compartment (225) of the first package (200) at least partially across the partition (240) toward the second compartment (230) of the first package (200).
- The package assembly according to Claim 5 further comprising a seal between the flange (240) and the first plastic film (215) of the first package (200) and a seal between the flange (240) and the second plastic film (220) of the first package (200).
- The package assembly according to Claim 1, wherein the second package (300) defines a flange (360) configured to extend across a partition (240) at least partially into the second compartment (230) of the first package (200), and
wherein the flange (360) is configured to serve as a conduit and direct the food additive (120) to the second compartment (230) in an instance in which the rupturable seal (335a) is ruptured. - A method of forming a package assembly for controlling a level of food additive, such as a marinade, imparted to a food product, such as meat, the method comprising:forming a support member of a first package (200) that includes a first compartment (225) configured substantially to contain a second package (300) and a second compartment (230) configured to contain a food product (110);forming the second package (300) configured to contain a food additive (120);loading the food additive (120) into the second package (300);sealing the food additive (120) in the second package (300) with at least a rupturable seal (335a) configured to rupture when exposed to a rupture pressure and allow the food additive (120) to escape the second package (300);loading the food product (110) into the second compartment (230) of the first package (200);loading the second package (300) substantially into the first compartment (225) of the first package (200) such that the second package (300) is in fluid communication with the second compartment (230) of the first package (200) upon a rupturing of the rupturable seal so as to allow the food additive (120) to mix with the food product (110); andsealing the support member of the first package (200) with a cover of the first package (200) such that the first package (200) is configured to withstand the rupture pressure and prevent leaking of the food additive (120) and food product (110) from the first package (200) during the mixing of the food additive (120) and the food product (110).
- The method according to Claim 10 further comprising applying a vacuum to the second package (300) during or prior to the sealing of the second package (300) and applying a vacuum to at least the second compartment (230) during or prior to the sealing of the first package (200).
- The method according to Claim 11, wherein the forming of the supporting member includes thermoforming a first plastic film (215) of the first package (200).
- The method according to Claim 12, wherein the forming of the second package (300) includes thermoforming a first plastic film (315) of the second package (300) into a support member of the second package (300) having an compartment of the second package (300).
- The method according to Claim 13, wherein loading the second package (300) at least partially into the first compartment (225) of the first package (200) includes positioning a flange (360) of the second package (300) at least partially across a partition (240) separating the first compartment (225) of the first package (200) and the second compartment (230) of the first package (200) such that the flange (360) extends from the first compartment (225) of the first package (200) toward the second compartment (230) of the first package (200).
- The method according to Claim 10, wherein the second package (300) defines a flange (360),
wherein loading the second package (300) at least partially into the first compartment (225) of the first package (200) comprises loading the second package (300) into the first package (200) such that the flange (360) of the second package (300) at least partially extends across a partition (240) into the second compartment (230), and
wherein the flange (360) is configured to serve as a conduit and direct the food additive (120) to the second compartment (230) in an instance in which the rupturable seal (335a) is ruptured.
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| US12/208,069 US7993692B2 (en) | 2008-09-10 | 2008-09-10 | Package assembly for on-demand marination and method for providing the same |
| PCT/US2009/053673 WO2010030464A1 (en) | 2008-09-10 | 2009-08-13 | Package assembly for on-demand marination and method for providing the same |
Publications (2)
| Publication Number | Publication Date |
|---|---|
| EP2321197A1 EP2321197A1 (en) | 2011-05-18 |
| EP2321197B1 true EP2321197B1 (en) | 2015-05-13 |
Family
ID=41066123
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20090791470 Not-in-force EP2321197B1 (en) | 2008-09-10 | 2009-08-13 | Package assembly for on-demand marination and method for providing the same |
Country Status (8)
| Country | Link |
|---|---|
| US (1) | US7993692B2 (en) |
| EP (1) | EP2321197B1 (en) |
| AU (1) | AU2009292100B2 (en) |
| BR (1) | BRPI0918141B1 (en) |
| CA (1) | CA2735407C (en) |
| ES (1) | ES2546405T3 (en) |
| MX (1) | MX2011002392A (en) |
| WO (1) | WO2010030464A1 (en) |
Families Citing this family (28)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| AU2004100000A4 (en) | 2004-01-02 | 2004-02-12 | Sands Innovations Pty Ltd | Dispensing stirring implement |
| AU2008210267B2 (en) * | 2007-01-31 | 2014-06-12 | Sands Innovations Pty Ltd | A dispensing utensil and manufacturing method therefor |
| AU2008365185B2 (en) | 2008-12-09 | 2016-05-05 | Sands Innovations Pty Ltd | A dispensing container |
| US20100290718A1 (en) * | 2009-05-15 | 2010-11-18 | Amber Laubacher | Frangible seals for multiple compartment bags, multiple compartment bags incorporating the same, and methods of forming the same |
| EP2435337B1 (en) | 2009-05-28 | 2020-09-02 | Ecolab USA Inc. | Method for aseptic packaging of food |
| JP5657662B2 (en) | 2009-07-26 | 2015-01-21 | フォエバー ヤング インターナショナル、 インク. | Instant self-heating container |
| US8511500B2 (en) | 2010-06-07 | 2013-08-20 | Sands Innovations Pty. Ltd. | Dispensing container |
| US20120006718A1 (en) * | 2010-07-09 | 2012-01-12 | Waldrop Christopher N | Packaging tray and method of use |
| ES1072775Y (en) * | 2010-07-13 | 2011-01-04 | Latre Jaime Jove | CONTAINER FOR FACIAL MASK |
| US8485360B2 (en) | 2011-03-04 | 2013-07-16 | Sands Innovations Pty, Ltd. | Fracturable container |
| US20120241336A1 (en) * | 2011-03-21 | 2012-09-27 | Cryovac, Inc. | On-Demand Marination Package |
| USD712250S1 (en) | 2012-09-10 | 2014-09-02 | The Hillshire Brands Company | Packaging for food product |
| USD704553S1 (en) | 2012-09-10 | 2014-05-13 | The Hillshire Brands Company | Packaging for food product |
| USD688942S1 (en) | 2012-09-10 | 2013-09-03 | The Hillshire Brands Company | Packaging for food product |
| USD705051S1 (en) | 2012-09-18 | 2014-05-20 | The Hillshire Brands Company | Packaging for food product |
| USD688921S1 (en) * | 2012-12-05 | 2013-09-03 | 3Rd Stone Design Inc. | Food container |
| US20140272094A1 (en) * | 2013-03-12 | 2014-09-18 | Advanced Food Systems, Inc. | Textured vegetable protein as a meat substitute and method and composition for making same |
| US20150376310A1 (en) * | 2014-06-26 | 2015-12-31 | E.I. Du Pont De Nemours And Company | Ethylene acid copolymers, their ionomers, and their use in packaging films and injection molded articles |
| WO2016022148A1 (en) * | 2014-08-08 | 2016-02-11 | Bemis Company, Inc. | Transparent retail bag-in-box package |
| USD764276S1 (en) * | 2015-05-05 | 2016-08-23 | World Centric | Container |
| US11150058B2 (en) * | 2016-04-06 | 2021-10-19 | Target Flares, LLC | Remote ignition device providing visual indication of a strike |
| CN107984844A (en) * | 2017-12-11 | 2018-05-04 | 杭州科能新材料科技有限公司 | A kind of sealed membrane for being applicable in packaging for foodstuff and preparation method thereof |
| CN108576783A (en) * | 2018-05-31 | 2018-09-28 | 西北农林科技大学 | A kind of instant noodles dry the application method of modifying agent and its emulsion and emulsion |
| USD905572S1 (en) * | 2019-02-07 | 2020-12-22 | Bradshaw International, Inc. | Combined lid and container |
| RU202937U1 (en) * | 2020-09-15 | 2021-03-15 | Общество с ограниченной ответственностью "ПАКГРАД" | MULTI-SECTION PLASTIC CONTAINER |
| USD983671S1 (en) | 2021-06-30 | 2023-04-18 | General Mills, Inc. | Dual compartment food container |
| USD1021618S1 (en) | 2022-05-13 | 2024-04-09 | General Mills, Inc. | Food packaging container |
| USD1078493S1 (en) * | 2025-03-31 | 2025-06-10 | Qingqing Liu | Sauce container |
Family Cites Families (142)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US180478A (en) * | 1876-08-01 | Method of heating gas for motive pother | ||
| US1303618A (en) * | 1919-05-13 | And apparatus for heating liquid by means of heat produced | ||
| US2733709A (en) * | 1956-02-07 | Sukacev | ||
| US654174A (en) * | 1899-01-05 | 1900-07-24 | Ernst Murmann | Heating appliance for canned food. |
| US628359A (en) * | 1899-04-29 | 1899-07-04 | Friedrich Schindler | Tin or can for containing canned foods. |
| US720435A (en) * | 1902-08-07 | 1903-02-10 | George Sidney Jewett | Heating-can for fruit or vegetables, &c. |
| US827222A (en) * | 1905-01-13 | 1906-07-31 | Wilhelm Espenhayn | Chemical heating device. |
| US1897723A (en) * | 1927-04-29 | 1933-02-14 | Walter H Free | Refrigerating device |
| US1751387A (en) * | 1928-09-22 | 1930-03-18 | Stanley M Bielek | Heating device |
| US1899286A (en) * | 1931-10-01 | 1933-02-28 | Kendall & Co | Container for chemical heating composition |
| US2112674A (en) * | 1935-12-13 | 1938-03-29 | Ind Dev And Res Lab Inc | Heat producing composition |
| US2265172A (en) | 1937-09-08 | 1941-12-09 | Hotcan Corp | Self-heating container |
| US2289008A (en) * | 1939-06-14 | 1942-07-07 | Interchem Corp | Food container |
| US2289007A (en) * | 1939-06-14 | 1942-07-07 | Interchem Corp | Heating mixture for food containers |
| US2245738A (en) * | 1940-02-14 | 1941-06-17 | Ivan M Taylor | Plural-compartment envelope |
| US2327447A (en) * | 1940-02-15 | 1943-08-24 | Continental Can Co | Self-heating food container |
| US2288895A (en) * | 1940-10-09 | 1942-07-07 | Continental Can Co | Self-heating container |
| US2300793A (en) | 1941-03-22 | 1942-11-03 | Virgil E C Martin | Self-heating can |
| US2613664A (en) | 1950-11-03 | 1952-10-14 | Eugene J Rivoche | Self-heating container having hermetic sealing means |
| US2620788A (en) | 1950-11-03 | 1952-12-09 | Eugene J Rivoche | Self-heating container |
| US2693793A (en) | 1951-08-06 | 1954-11-09 | Ray L Steven | Pressure cooker |
| US2916886A (en) | 1956-06-15 | 1959-12-15 | Kwik Kold Of America Inc | Unit type chemical freezing package |
| US2968932A (en) * | 1958-07-31 | 1961-01-24 | John R Vance | Cooling device |
| US3328136A (en) * | 1964-03-18 | 1967-06-27 | Verlam Distributors Inc | Composition for producing heat |
| US3542032A (en) | 1968-03-22 | 1970-11-24 | Cramer Products Inc | Therapy package |
| DE6946391U (en) | 1969-11-29 | 1970-05-14 | Koellner Sigrune | MULTI-CHAMBER CONTAINER FOR THE SEPARATE ACCOMMODATION OF REACTING SUBS ANZES FOR THE MANUFACTURING OF READY-TO-USE DENTAL PREPARATIONS. |
| US3812043A (en) * | 1970-10-30 | 1974-05-21 | Du Pont | Package for dispensing an ice-removing composition |
| FR2142726A1 (en) | 1971-06-24 | 1973-02-02 | Sedimm | |
| US3970068A (en) * | 1973-05-29 | 1976-07-20 | Shotaro Sato | Heat exchange package for food |
| US3865117A (en) * | 1973-06-25 | 1975-02-11 | Micro Bio Medics Inc | Thermal compress and method and apparatus for making the same |
| US3983994A (en) | 1975-01-29 | 1976-10-05 | Ihor Wyslotsky | Flexible package |
| US4064296A (en) | 1975-10-02 | 1977-12-20 | W. R. Grace & Co. | Heat shrinkable multi-layer film of hydrolyzed ethylene vinyl acetate and a cross-linked olefin polymer |
| GB1580187A (en) | 1976-06-03 | 1980-11-26 | Grace W R & Co | Flexible envelopes |
| US4281418A (en) * | 1978-02-07 | 1981-08-04 | Stanley Cieslak | Portable furnace for wearing apparel |
| US4278738A (en) * | 1978-03-10 | 1981-07-14 | W. R. Grace & Co. | Ethylene-vinyl acetate copolymer film laminate |
| BE894377A (en) | 1982-09-13 | 1983-01-03 | Staar Dev Cy S A | Multicompartment food packs of thermo-formed film - with internal seams which can be parted to mix or release the contents |
| US4510919A (en) * | 1982-11-05 | 1985-04-16 | Simon Benmussa | Self heating receptacle |
| IT1189434B (en) * | 1982-12-07 | 1988-02-04 | Grog Srl | DISPOSABLE DEVICE FOR SELF-HEATING OR SELF-COOLING OF BEVERAGES AND FOODS THROUGH AN EXOTHERMAL OR ENDOTHERMAL REACTION |
| US4640264A (en) * | 1983-10-20 | 1987-02-03 | Tosinobu Yamaguchi | Food and drink warming container |
| DE3425419C2 (en) * | 1984-07-10 | 1993-12-09 | Zeolith Tech | Adiabatic heating and cooling devices based on the adsorption principle |
| US4573447A (en) * | 1985-02-19 | 1986-03-04 | Sunbelt America Corporation | Chemical heater |
| JPS61253023A (en) * | 1985-04-04 | 1986-11-10 | 旭化成株式会社 | Heating container |
| JPS6273062A (en) * | 1985-09-25 | 1987-04-03 | 右近 村次郎 | Can in which drinking water or food is self-heated or self-cooled by exothermic or endothermic reaction |
| FR2598070B1 (en) * | 1986-05-05 | 1989-05-19 | Labrousse Bernard | SINGLE USE HEAT TRANSFER PACKAGING FOR BEVERAGES, FOODS AND MEDICINES |
| US4793323A (en) | 1986-07-16 | 1988-12-27 | Blusei S.P.A. | Single-use self-heating container for liquids and/or solids |
| US4838242A (en) * | 1986-07-28 | 1989-06-13 | Oblon Ronald P | Device for changing temperature of material therein |
| US4722323A (en) * | 1986-07-28 | 1988-02-02 | Oblon Ronald P | Device for changing temperature of material therein |
| FR2602752B1 (en) * | 1986-08-12 | 1988-11-10 | Oreal | SET FOR SEPARATE PACKAGING OF AT LEAST TWO PRODUCTS WHICH MUST BE IN CONTACT ONLY AT THE TIME OF USE AND FOR THE REALIZATION OF THIS CONTACT |
| FR2607692B1 (en) * | 1986-12-05 | 1989-03-31 | Charvin Guy | SELF-CONTAINED DEVICES FOR HEATING FOOD CONTAINERS |
| US4879430A (en) | 1987-05-14 | 1989-11-07 | Plicon Corporation | Patterned adherent film structures and process for making |
| FR2642726B1 (en) * | 1989-02-07 | 1991-06-14 | Monoplast | MULTI-COMPARTMENT TRAY |
| US4989729A (en) * | 1989-06-01 | 1991-02-05 | Huang Kin Shen | Automatic rapid heating can |
| US5035230A (en) * | 1990-02-23 | 1991-07-30 | Steidl Gary V | Disposable food heater |
| US5167973A (en) | 1990-08-14 | 1992-12-01 | Snyder William D | Comestibles container |
| US5168708A (en) | 1991-09-23 | 1992-12-08 | Israel Siegel | Disposable and reusable valveless sorption self-cooling and self-heating containers |
| US5220909A (en) * | 1992-05-28 | 1993-06-22 | The United States Of America As Represented By The Secretary Of The Army | Self-heating individual meal module |
| US5209348A (en) * | 1992-06-04 | 1993-05-11 | James D. Schafer | Cereal bowl with separate self-contained cereal and milk compartments |
| US5351675A (en) | 1992-08-14 | 1994-10-04 | The Kendall Company | Method and apparatus for preheating an optical instrument prior to use thereof in a medical procedure |
| US5376120A (en) | 1992-10-21 | 1994-12-27 | Biomet, Inc. | Biocompatible implant and method of using same |
| US5287961A (en) * | 1992-10-23 | 1994-02-22 | W.R. Grace & Co.-Conn. | Multi-compartment package having improved partition strip |
| US5392762A (en) * | 1994-01-24 | 1995-02-28 | Hsu; Yu T. | Beverage can heating device |
| US5388565A (en) * | 1994-04-01 | 1995-02-14 | Ou; Lih-Horng | Self-heating container system |
| US5626022A (en) | 1994-05-31 | 1997-05-06 | Insta-Heat, Inc. | Container with integral module for heating or cooling the contents |
| US5465707A (en) | 1994-06-15 | 1995-11-14 | Fulcher; Fred | Self heating individual meal package |
| US5517981A (en) * | 1994-06-21 | 1996-05-21 | The United States Of America As Represented By The Secretary Of The Army | Water-activated chemical heater with suppressed hydrogen |
| US5514394A (en) * | 1994-07-29 | 1996-05-07 | Lenahan; Robert F. | Cereal package |
| US5483949A (en) * | 1994-09-22 | 1996-01-16 | James; Dean B. | Exothermic compositions and container for heating food |
| US5542418A (en) * | 1995-01-30 | 1996-08-06 | Hotcan International, Ltd. | Acid-base fuels for self heating food containers |
| US5486371A (en) * | 1994-09-26 | 1996-01-23 | Chen; Chung-Te | Method for cooking food with heat energy generated from natural stone materials |
| US5496575A (en) * | 1994-11-18 | 1996-03-05 | Newarski; Emil | Single use cereal and milk container |
| US5686127A (en) * | 1995-06-06 | 1997-11-11 | W. R. Grace & Co.-Conn. | Dual web package having improved gaseous exchange |
| CA2152452C (en) * | 1995-06-22 | 1998-02-03 | Robert Freiman | Self heating container |
| US5662096A (en) | 1995-07-03 | 1997-09-02 | Omni Therm, Inc. | Trigger to activate supercooled aqueous salt solution for use in a heat pack |
| FR2758795B1 (en) | 1997-01-24 | 1999-02-26 | Oreal | PACKAGING FOR LIQUID TO SEMI-LIQUID PRODUCT |
| FR2766148B1 (en) * | 1997-07-16 | 1999-09-17 | Soc D Const De Materiel Metall | TROLLEY COMPRISING A COOLING DEVICE THAT CAN BE INSTALLED AT ANY TIME CHOSEN BY THE USER AND METHOD FOR PROVIDING A HEATED FOOD |
| US6712201B1 (en) | 1998-03-13 | 2004-03-30 | Sealed Air Corporation | Foam in bag packaging system and method for producing the same |
| US5915461A (en) * | 1998-03-31 | 1999-06-29 | Deroyal Industries, Inc. | Heat pack and trigger apparatus |
| DE29814215U1 (en) * | 1998-08-12 | 1998-10-15 | Klocke Verpackungs-Service GmbH, 76356 Weingarten | Multi-chamber container |
| GB9827718D0 (en) | 1998-12-16 | 1999-02-10 | Thermotic Dev Ltd | Improvements in or relating to fluid containers |
| GB9904357D0 (en) * | 1999-02-26 | 1999-04-21 | Richardson Robert N | Improvements to beverage and other containers |
| US6393843B2 (en) * | 1999-03-06 | 2002-05-28 | Allegiance Corporation | Extended life thermal pack |
| US6341602B1 (en) * | 1999-03-09 | 2002-01-29 | Fred Fulcher | Package for flameless heating and heater for the package |
| US6178753B1 (en) * | 1999-04-19 | 2001-01-30 | Ontro, Inc. | Container with self-heating module having liquid reactant and breakable reactant barrier at distal end of module |
| US6289889B1 (en) | 1999-07-12 | 2001-09-18 | Tda Research, Inc. | Self-heating flexible package |
| AU7545800A (en) | 1999-10-06 | 2001-05-10 | Thermotic Developments Limited | Self-heating or self-cooling containers |
| US7021848B1 (en) * | 1999-10-08 | 2006-04-04 | The Procter & Gamble Company | Semi-enclosed applicator having a temperature changing element |
| US6726386B1 (en) * | 1999-10-08 | 2004-04-27 | The Procter & Gamble Company | Semi-enclosed applicator and a cleaning composition contained therein |
| US6079405A (en) * | 1999-11-30 | 2000-06-27 | Justo; Jose A. | Container with in situ dual food product mixing and heating |
| JP2001171755A (en) * | 1999-12-14 | 2001-06-26 | Hosokawa Yoko Co Ltd | Packaging container |
| US6334488B1 (en) * | 2000-01-11 | 2002-01-01 | Weatherford/Lamb, Inc. | Tubing plug |
| DE10003534A1 (en) | 2000-01-27 | 2001-08-16 | Ebbecke Reinhard | Disposable containers for heating and cooling liquids |
| US6338252B1 (en) * | 2000-03-13 | 2002-01-15 | Smartcup International | Heat transfer container |
| WO2001087090A1 (en) * | 2000-05-12 | 2001-11-22 | The Board Of Regents Of The University Of Nebraska | Methods and compositions to enhance tenderness and value of meat |
| DE10032799B4 (en) * | 2000-06-28 | 2005-09-22 | Coty B.V. | Multi-chamber packaging for cooling or heating products |
| US7235187B2 (en) * | 2000-07-13 | 2007-06-26 | The Procter & Gamble Company | Methods and apparatuses for delivering a volatile component via a controlled exothermic reaction |
| US7081211B2 (en) * | 2000-07-13 | 2006-07-25 | The Procter & Gamble Company | Multi-layer reaction mixtures and apparatuses for delivering a volatile component via a controlled exothermic reaction |
| US6234165B1 (en) * | 2000-08-28 | 2001-05-22 | Kevin A. Creighton | Baby bottle warmer |
| US6564558B1 (en) * | 2000-10-05 | 2003-05-20 | Seymour Michael L | Disposable self-cooling, self-heating container |
| US6547063B1 (en) * | 2000-10-10 | 2003-04-15 | The Procter & Gamble Company | Article for the delivery of foam products |
| US6484514B1 (en) | 2000-10-10 | 2002-11-26 | The Procter & Gamble Company | Product dispenser having internal temperature changing element |
| GB0026605D0 (en) * | 2000-10-31 | 2000-12-13 | Bush Boake Allen Ltd | Compartmentalized storage system |
| US6601577B2 (en) * | 2001-04-06 | 2003-08-05 | Moshe Bouskila | Container assembly for warming beverages and method of forming and using it |
| US6743451B2 (en) * | 2001-04-16 | 2004-06-01 | H. J. Heinz Company | Resealable bag with arcuate rupturable seal |
| GB0110050D0 (en) | 2001-04-24 | 2001-06-13 | Thermotic Dev Ltd | Steam generator |
| US6962149B2 (en) | 2001-05-02 | 2005-11-08 | Expressasia.Com Snd. Bhd. | Insertable thermotic module for self-heating can |
| CA2346223C (en) | 2001-05-25 | 2002-12-10 | Ivan Sestak | Self heating pre-moistened wipe(s) package |
| JP2004534699A (en) * | 2001-06-29 | 2004-11-18 | ザ プロクター アンド ギャンブル カンパニー | Self-heating / self-cooling package |
| IL144939A0 (en) | 2001-08-16 | 2002-06-30 | Convenience Heating Technologi | Disposable self-heating container |
| US6635077B2 (en) | 2001-09-07 | 2003-10-21 | S.C. Johnson Home Storage, Inc. | Structure including a film material |
| US6935492B1 (en) * | 2002-01-26 | 2005-08-30 | Barry Alan Loeb | Flexible mixing pouch with aseptic burstable internal chambers |
| US6601576B1 (en) * | 2002-03-15 | 2003-08-05 | Kenneth E. Baysinger, Jr. | Bottle warming apparatus |
| US6698504B2 (en) * | 2002-04-16 | 2004-03-02 | Andrew E. Briesmeister | Apparatus and process for more rapidly cooling products contained in pouched or flexible containers |
| ATE395273T1 (en) * | 2002-05-17 | 2008-05-15 | Crown Packaging Technology Inc | SELF HEATING/COOLING CONTAINER |
| EP1362537A1 (en) * | 2002-05-17 | 2003-11-19 | Crown Cork & Seal Technologies Corporation | Self heating or cooling container |
| US20040181451A1 (en) | 2002-08-27 | 2004-09-16 | The Procter & Gamble Company | Methods relating to multi-compartment laundry products |
| DE10243401B4 (en) * | 2002-09-18 | 2004-07-29 | Voco Gmbh | Packaging for storing substances and method for producing a directly applicable mixture of two substances from this packaging |
| US6726364B2 (en) | 2002-09-19 | 2004-04-27 | Poppack, Llc | Bubble-seal apparatus for easily opening a sealed package |
| US6827080B2 (en) * | 2002-10-03 | 2004-12-07 | Kimberly-Clark Worldwide, Inc. | Pressure activated reaction vessel and package |
| US6766797B1 (en) * | 2003-04-10 | 2004-07-27 | The United States Of America As Represented By The Secretary Of The Army | Method for making a disposable package for an agent activatable substance and a package made thereby |
| US6902335B2 (en) * | 2003-05-08 | 2005-06-07 | R.P. Scherer Technologies, Inc. | Hand held dispensing and application apparatus |
| US6920873B2 (en) * | 2003-09-11 | 2005-07-26 | Energy Conversion Devices, Inc. | Portable heating pack |
| KR20060107534A (en) | 2003-10-17 | 2006-10-13 | 이노포스 인코퍼레이티드 | Heat-generating integrated body, flameless heater and self-heating packaging using same |
| US7243788B2 (en) * | 2003-10-22 | 2007-07-17 | Kimberly-Clark Worldwide, Inc. | Package for segregating and mixing substances |
| US7025055B2 (en) * | 2004-03-15 | 2006-04-11 | Ontech Delaware Inc. | Tray for selectably heating or cooling the contents |
| US20060162344A1 (en) * | 2004-03-15 | 2006-07-27 | Ontech Delaware Inc. | Container with module for heating or cooling the contents |
| US20060169276A1 (en) * | 2004-03-15 | 2006-08-03 | Ontech Delaware Inc. | Tray for selectably heating or cooling the contents |
| US7117684B2 (en) | 2004-03-15 | 2006-10-10 | Ontech Delaware Inc. | Container with integral module for heating or cooling the contents |
| US7311660B2 (en) | 2004-04-16 | 2007-12-25 | Ricardo Alexander Gomez | Method and apparatus for heating and applying warm antifog solution to endoscopes as well as a distal lens protector |
| US7371268B2 (en) * | 2004-04-23 | 2008-05-13 | Bendix Commercial Vehicle Systems Llc | Filter with thermal vent |
| US20050235653A1 (en) | 2004-04-26 | 2005-10-27 | Avista Technologies, Llp | Temperature changng package |
| US20060005827A1 (en) * | 2004-05-04 | 2006-01-12 | Candle Corporation Of America | Heater product, system and composition |
| US20050279106A1 (en) | 2004-06-17 | 2005-12-22 | Leonzo Fernando O | Self-heating/cooling arrangement for beverage and/or food |
| DE202004014511U1 (en) * | 2004-09-17 | 2004-11-25 | Klocke Verpackungs-Service Gmbh | Multi-chamber packaging |
| US20060260326A1 (en) | 2005-05-20 | 2006-11-23 | Hickey Charles P | Heating and cooling device with replaceable cartridge for beverage containers |
| CN101031228A (en) | 2005-05-30 | 2007-09-05 | 村上正人 | Liquid heating container |
| GB0512889D0 (en) | 2005-06-24 | 2005-08-03 | Steamfast Europ Ltd | Improvement in or relating to containers for cooking foodstuffs |
| US20070089730A1 (en) * | 2005-10-24 | 2007-04-26 | Gunz Gregory L | Khem-gz |
| WO2007059151A2 (en) * | 2005-11-14 | 2007-05-24 | Heat Wave Technologies Llc | Improved self-heating container |
| TWM294500U (en) * | 2005-12-02 | 2006-07-21 | Yung Shin Pharm Ind Co Ltd | Separated double-bag structure enabling easy mixing of its contained medicines, substances, or the likes |
| US7940908B2 (en) | 2006-02-23 | 2011-05-10 | Qualcomm Incorporated | Sharing profile data between telecommunication devices |
| US20080178865A1 (en) * | 2007-01-05 | 2008-07-31 | Shelley Retterer | Portable beverage bottle heaters and coolers |
| BRPI0809438A2 (en) * | 2007-03-27 | 2015-06-16 | Cryovac Inc | Package to make juicy meat on demand |
-
2008
- 2008-09-10 US US12/208,069 patent/US7993692B2/en active Active
-
2009
- 2009-08-13 AU AU2009292100A patent/AU2009292100B2/en not_active Ceased
- 2009-08-13 CA CA2735407A patent/CA2735407C/en active Active
- 2009-08-13 ES ES09791470.9T patent/ES2546405T3/en active Active
- 2009-08-13 EP EP20090791470 patent/EP2321197B1/en not_active Not-in-force
- 2009-08-13 WO PCT/US2009/053673 patent/WO2010030464A1/en not_active Ceased
- 2009-08-13 BR BRPI0918141-5A patent/BRPI0918141B1/en not_active IP Right Cessation
- 2009-08-13 MX MX2011002392A patent/MX2011002392A/en active IP Right Grant
Also Published As
| Publication number | Publication date |
|---|---|
| US20100062130A1 (en) | 2010-03-11 |
| BRPI0918141A2 (en) | 2015-12-01 |
| ES2546405T3 (en) | 2015-09-23 |
| AU2009292100A1 (en) | 2010-03-18 |
| BRPI0918141B1 (en) | 2019-11-05 |
| WO2010030464A1 (en) | 2010-03-18 |
| US7993692B2 (en) | 2011-08-09 |
| CA2735407C (en) | 2013-12-31 |
| CA2735407A1 (en) | 2010-03-18 |
| MX2011002392A (en) | 2011-04-12 |
| AU2009292100B2 (en) | 2013-07-11 |
| EP2321197A1 (en) | 2011-05-18 |
| WO2010030464A8 (en) | 2010-11-04 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US7993692B2 (en) | Package assembly for on-demand marination and method for providing the same | |
| AU2008231374B2 (en) | On-demand meat tenderizing package | |
| US3573069A (en) | Combination frozen food and breading composition package | |
| US5629060A (en) | Packaging with peelable lid | |
| US5050736A (en) | Reclosable package | |
| ES2522284T3 (en) | Vacuum foil container, microwave heated, detachable, self-ventilated | |
| TWI616380B (en) | Packing bag | |
| US5843500A (en) | Bacon wrapped seafood package and process | |
| US20120241336A1 (en) | On-Demand Marination Package | |
| US5157901A (en) | Method for sealing retort container | |
| Mazzola et al. | Packaging Design Alternatives for | |
| JP2549842B2 (en) | Manufacturing method of heat-sterilized solid food containers | |
| AU2012231017A1 (en) | On-demand marination package | |
| US20240262599A1 (en) | Nested heat-sealable bags for food storage | |
| JP3950803B2 (en) | Food packaging bags | |
| JPS6049772A (en) | Packed product of unshelled shellfish | |
| JP2005162278A (en) | Manufacturing method for packaging container and packaging container | |
| US20070031550A1 (en) | Method for continuously processing meat substrates | |
| JP2006021820A (en) | Microwave cooking bag and cooked food for microwave oven | |
| JP2003252380A (en) | Crustacean package and manufacturing method therefor | |
| JPH076136Y2 (en) | Packaging bag | |
| JP2017214072A (en) | Food product packaging container | |
| JP2015221678A (en) | Food packaging bag | |
| JP2005126130A (en) | Method for manufacturing packaging container and packaging container | |
| JPH09207972A (en) | Multi-sectional packaging body available for heating by microwave oven |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| 17P | Request for examination filed |
Effective date: 20110301 |
|
| AK | Designated contracting states |
Kind code of ref document: A1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| AX | Request for extension of the european patent |
Extension state: AL BA RS |
|
| DAX | Request for extension of the european patent (deleted) | ||
| 17Q | First examination report despatched |
Effective date: 20120803 |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20140606 |
|
| RIN1 | Information on inventor provided before grant (corrected) |
Inventor name: FINLEY, DAVID, M. Inventor name: MILLWOOD, TERRY Inventor name: CARROUTH, ANDREW, BOYD, JR. Inventor name: CONNER, HOWARD, DEAN |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| INTG | Intention to grant announced |
Effective date: 20141203 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HR HU IE IS IT LI LT LU LV MC MK MT NL NO PL PT RO SE SI SK SM TR |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: REF Ref document number: 726738 Country of ref document: AT Kind code of ref document: T Effective date: 20150615 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R096 Ref document number: 602009031251 Country of ref document: DE Effective date: 20150625 |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2546405 Country of ref document: ES Kind code of ref document: T3 Effective date: 20150923 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK05 Ref document number: 726738 Country of ref document: AT Kind code of ref document: T Effective date: 20150513 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MG4D |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150914 Ref country code: LT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: NO Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150813 Ref country code: HR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: FI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LV Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: GR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150814 Ref country code: IS Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150913 Ref country code: AT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: BG Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150813 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 7 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: EE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: DK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R097 Ref document number: 602009031251 Country of ref document: DE |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PL Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: CZ Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: RO Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150513 Ref country code: SK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150813 Ref country code: MC Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| 26N | No opposition filed |
Effective date: 20160216 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150831 Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MM4A |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150813 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 8 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: BE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150813 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MT Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SM Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: HU Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT; INVALID AB INITIO Effective date: 20090813 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SE Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 9 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: TR Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20150813 |
|
| PGRI | Patent reinstated in contracting state [announced from national office to epo] |
Ref country code: IT Effective date: 20170710 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MK Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20150513 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 10 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20190826 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: DE Payment date: 20190828 Year of fee payment: 11 Ref country code: ES Payment date: 20190902 Year of fee payment: 11 Ref country code: IT Payment date: 20190826 Year of fee payment: 11 Ref country code: FR Payment date: 20190826 Year of fee payment: 11 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: GB Payment date: 20190827 Year of fee payment: 11 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R119 Ref document number: 602009031251 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MM Effective date: 20200901 |
|
| GBPC | Gb: european patent ceased through non-payment of renewal fee |
Effective date: 20200813 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: DE Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20210302 Ref country code: FR Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200831 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: GB Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200813 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: NL Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200901 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20220110 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: ES Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200814 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: IT Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20200813 |