EP1371502B1 - Machine for rounding the corners of hard covers for books - Google Patents
Machine for rounding the corners of hard covers for books Download PDFInfo
- Publication number
- EP1371502B1 EP1371502B1 EP20030007728 EP03007728A EP1371502B1 EP 1371502 B1 EP1371502 B1 EP 1371502B1 EP 20030007728 EP20030007728 EP 20030007728 EP 03007728 A EP03007728 A EP 03007728A EP 1371502 B1 EP1371502 B1 EP 1371502B1
- Authority
- EP
- European Patent Office
- Prior art keywords
- die
- cover
- machine
- covers
- sharp
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
Images



Classifications
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42C—BOOKBINDING
- B42C7/00—Manufacturing bookbinding cases or covers of books or loose-leaf binders
-
- B—PERFORMING OPERATIONS; TRANSPORTING
- B42—BOOKBINDING; ALBUMS; FILES; SPECIAL PRINTED MATTER
- B42C—BOOKBINDING
- B42C5/00—Preparing the edges or backs of leaves or signatures for binding
- B42C5/02—Preparing the edges or backs of leaves or signatures for binding by rounding or backing
Definitions
- the present invention relates to a machine for rounding the sharp corners of hard covers to be applied to books of various types, such as diaries and daybooks.
- GB 961258 shows such a machine.
- Covers of this type comprise a cardboard core clad externally with a cladding sheet, the edges of which are folded over for a certain depth onto the inner face of the cover and glued.
- the cladding sheet is normally of glossy paper, balacron, or other suitable materials requested by the market, to give a more pleasing appearance and greater prestige to the relative book.
- the corners of the cover of books of the aforesaid type are often rounded, both to give the book a more precise appearance, and to enable the product to conform to Community directives, which prescribe the elimination of sharp corners from the covers of books intended for young children.
- a cover with rounded corners is obtained by starting with a cover with sharp corners, as would emerge from a traditional cover-forming machine, i.e. in the form of a cardboard rectangle to which said cladding sheet has been applied. Using a suitable tool, an operator folds a part of each sharp corner of the cover towards that side of the cover which is to remain on the inside of the book, then finally compressing said folded cover part with force so as to flatten it and hence eliminate the sharp corner. As will be apparent, all this significantly affects the production costs of the relative book.
- the object of the present invention is therefore to provide a machine able to transform the sharp cornered covers produced by a conventional cover-forming machine into covers with rounded corners.
- the forming die is incomplete, in the sense that it comprises four spaced-apart coplanar portions, which each involve only one relative corner part of the cover.
- the means for extracting the cover from the die consist in this latter case of means which enable the four portions of the die to be withdrawn, each in the direction of a bisector of the relative corner of the cover.
- the machine 10 comprises a metal structure 12 carrying a first belt conveyor device for feeding sharp cornered covers (not shown for simplicity in this figure) in succession, in the direction of the arrow A, to a rounding station, the position of which in the machine 10 is indicated only generically in Figure 1 (with the aid of an embracing bracket and the reference numeral 16).
- This rounding station is shown in Figures 2 and 3 .
- the covers fed to the machine 10 (which are partially visible in Figures 5, 6 and 7 where they are indicated by 28) are sharp cornered, originating from a conventional cover-forming machine (not shown) disposed downstream of the machine 10 (i.e. to the right in Figure 1 ).
- a second conveyor device comprising a lower belt conveyor 20 opposite which there are two upper belt conveyors 22.1 and 22.2, disposed symmetrically about the rounding station 16.
- the covers pass between these conveyors 22.1, 22.2 and the lower conveyor 20.
- a rigid table 24 ( Figures 1 and 3 ) presenting longitudinal grooves 26 ( Figure 3 ) in which the upper branches of the belts 20.1 and 20.2 of the lower conveyor 20 pass, the upper edge of these belts projecting slightly from the upper surface of the table 24.
- This latter and the lower conveyor 20 can be lowered together, to pass from the level of Figure 1 (corresponding to the level of the table in Figure 5.1 ), which enables the covers 28 to be moved, to a lower level visible in Figures 6.2 and 7.2 .
- the table 24 and the lower conveyor 20 are lowered by a device 30 comprising a pneumatic operating cylinder 32 ( Figure 1 ).
- a device 30 comprising a pneumatic operating cylinder 32 ( Figure 1 ).
- the lower conveyor 20 is driven by a motorized roller 38 which transmits its rotary movement to the conveyor 20 by friction via an idle intermediate roller 40 rigid with the table 24. Consequently, when the table 24 is lowered together with the lower conveyor 20, the transmission of movement from the motorized roller 38 to the intermediate roller 40 ceases automatically, the conveyor 20 hence halting.
- a die indicated overall by 42, is present but in this specific case is incomplete in the sense that it comprises four separate portions (42.1, 42.2, 42.3, 42.4), each of which is arranged to receive one of the four corner parts of a cover 28( Figures 5.1 and 5.2 ).
- the portions (42.1-42.4) of the die 42 are shown very schematically in Figures 2 and 4 , but in greater detail in Figures 5, 6 and 7 .
- the portions 42.1-42.4 are coplanar and aligned in opposing pairs.
- the two portions 42.1 and 42.3 or 42.2 and 42.4 of each pair can be moved away from or towards each other (as indicated by the double arrows B in Figure 3 ) along a bisector of a relative corner of a cover 28 lying in the rounding station 16.
- the portions 42.1-42.4 are in their closest or working position (which is assumed just after a cover 28 comes to rest - by virtue of the stop elements 36 - in the rounding station 16)
- the relative cover 28, or rather its corresponding corner part lies in the situation shown by Figures 5.1 and 5.2 .
- Movement of the four portions 42.1-42.4 in the direction of the arrows B is achieved by relative pneumatic cylinder devices 48 fixed to the aforesaid support plate 50, which is slidable on longitudinal guides 82 provided in a plate 84 carried by the structure 12.
- the portions 42.1-42.4 of the die 42 are provided with an undercut 70 which enables each sharp corner of a cover 28 to rest on the relative step 72.
- two stop elements 36 ( Figure 3 ), symmetrically disposed one on each side of the table 24, project upwards beyond the upper surface thereof.
- the stop elements 36 form part of a relative stop device indicated by 34 and rigid with the portions 42.1 and 42.2 respectively. Consequently, when these portions of the die 42 are in their closest (working) position, the covers 28 which transit on the lower conveyor 20 interfere with the stop elements 36, to halt in the rounding station 16.
- the machine 10 presents a press-punch unit (one of these units is shown in Figure 4 and indicated overall by 46) carried by the structure 12 of the machine 10.
- the unit 46 comprises a press 54 and a punch 56, which are carried by a support element 60 slidable along a vertical column 58 and fixed to the lower end of the piston rod 62 of a pneumatic cylinder device 52.
- both the press 54 and the punch 56 can be moved rigidly in the two senses in the direction of the double arrow C of Figure 4 .
- the cover 28 is in the position shown in Figures 5.1 and 5.2 , the press 54 and punch 56 can be lowered simultaneously.
- the press 54 is the first to come into contact with the cover 28, so that this latter is forced downwards. Simultaneously the table 24, together with the lower conveyor 20, is lowered to pass from its level of Figure 5.2 to its level of Figure 6.2 . This enables the press 54 both to continue its downward stroke and press the cover 28 against the sunken part 66 of the die 42, and to halt the lower conveyor 20 to prevent its belts 20.1 and 20.2 rubbing against the cover 28 and spoiling its cladding.
- the sunken part, or base, of the die 42 is formed in this specific case by the bottom surface 66 of the relative portion 42.1-42.4 and by the upper surface of the table 24 in the situation shown in Figures 6.1 and 6.2 . As can be seen from these figures, the relative sharp corner of the cover 28 is folded upwards (as indicated by the reference numeral 29).
Landscapes
- Engineering & Computer Science (AREA)
- Mechanical Engineering (AREA)
- Manufacturing & Machinery (AREA)
- Bending Of Plates, Rods, And Pipes (AREA)
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Presses And Accessory Devices Thereof (AREA)
- Making Paper Articles (AREA)
Description
- The present invention relates to a machine for rounding the sharp corners of hard covers to be applied to books of various types, such as diaries and daybooks.
GB 961258 - Covers of this type comprise a cardboard core clad externally with a cladding sheet, the edges of which are folded over for a certain depth onto the inner face of the cover and glued. The cladding sheet is normally of glossy paper, balacron, or other suitable materials requested by the market, to give a more pleasing appearance and greater prestige to the relative book.
- The corners of the cover of books of the aforesaid type are often rounded, both to give the book a more precise appearance, and to enable the product to conform to Community directives, which prescribe the elimination of sharp corners from the covers of books intended for young children.
- Traditionally, a cover with rounded corners is obtained by starting with a cover with sharp corners, as would emerge from a traditional cover-forming machine, i.e. in the form of a cardboard rectangle to which said cladding sheet has been applied. Using a suitable tool, an operator folds a part of each sharp corner of the cover towards that side of the cover which is to remain on the inside of the book, then finally compressing said folded cover part with force so as to flatten it and hence eliminate the sharp corner. As will be apparent, all this significantly affects the production costs of the relative book.
- Improved cover-forming machines have been constructed which are also able to directly produce cardboard covers provided with rounded corners. However for this purpose, these machines are fed with rectangular cardboard cores which have to be previously punched so as to present the corners already rounded, and with the cladding sheets also already punched to present in each of their corners an indentation which enables the cladding sheet to be folded onto the inside of the cover to follow the corresponding corner rounding of the core.
- It is immediately apparent that high costs are also involved in this case. The object of the present invention is therefore to provide a machine able to transform the sharp cornered covers produced by a conventional cover-forming machine into covers with rounded corners.
- This object is attained by the machine according to the present invention, comprising:
- a forming die presenting a sunken part having, in plan view, substantially the length and width of the sharp cornered cover, the sunken part of the die presenting however rounded corners having the same profile as those which are to be obtained for the cover;
- pressing means for pressing the cover to its full extent within the die sunken part except in the regions comprising its sharp corners, so that these latter become folded outwards, the completely clad face of the cover facing inwards;
- punch means, the plan profile of which partly matches the rounded profile of the rounded corners of the die sunken part, to press each folded corner of the cover against the die sunken part;
- means for extracting the cover, which now presents its corners rounded, from the die.
- Preferably the forming die is incomplete, in the sense that it comprises four spaced-apart coplanar portions, which each involve only one relative corner part of the cover. Conveniently the means for extracting the cover from the die consist in this latter case of means which enable the four portions of the die to be withdrawn, each in the direction of a bisector of the relative corner of the cover.
- The invention will be more apparent from the ensuing description of one embodiment thereof given by way of example. In this description reference is made to the accompanying drawings, in which:
-
Figure 1 is a schematic partial elevation view of a machine according to the present invention; -
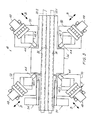
Figure 2 is a plan view from above of the rounding station of the machine, showing the four portions which comprise the forming die; -
Figure 3 is a partial enlargement of the preceding figure, with the elimination of certain parts and the addition of others; -
Figure 4 is an elevational view of a press-punch unit in the direction of the arrow F ofFigure 3 ; -
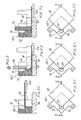
Figures 5.1 and 5.2 are respectively a plan view and a vertical section on the line 5-5 ofFigure 5.1 , of one of the four portions of the die, with the cover resting on them at its corresponding sharp corner; - Figures 6.21 and
6.2 are respectively a plan view and a vertical section on the line 6-6 ofFigure 6.1 , of one of the four portions of the die, with the cover forced by the press (visible, as is the punch, only inFigure 6.2 ) into the die and against its sunken part, the relative sharp corner of the cover being folded upwards; -
Figures 7.1 and 7.2 are respectively a plan view and a vertical section on the line 7-7 ofFigure 7.1 , of one of the four portions of the die, the folded corner of the cover being flattened by the action of a punch (visible, as is the press, only inFigure 7.2 ); - Figure 8 is a cross-section through the punch.
- As can be seen from
Figure 1 , themachine 10 comprises ametal structure 12 carrying a first belt conveyor device for feeding sharp cornered covers (not shown for simplicity in this figure) in succession, in the direction of the arrow A, to a rounding station, the position of which in themachine 10 is indicated only generically inFigure 1 (with the aid of an embracing bracket and the reference numeral 16). This rounding station is shown inFigures 2 and3 . The covers fed to the machine 10 (which are partially visible inFigures 5, 6 and 7 where they are indicated by 28) are sharp cornered, originating from a conventional cover-forming machine (not shown) disposed downstream of the machine 10 (i.e. to the right inFigure 1 ). - In correspondence with the
rounding station 16 there is provided a second conveyor device, indicated overall by 18 (Figure 1 ), comprising alower belt conveyor 20 opposite which there are two upper belt conveyors 22.1 and 22.2, disposed symmetrically about therounding station 16. The covers pass between these conveyors 22.1, 22.2 and thelower conveyor 20. In correspondence with therounding station 16 there is also provided a rigid table 24 (Figures 1 and3 ) presenting longitudinal grooves 26 (Figure 3 ) in which the upper branches of the belts 20.1 and 20.2 of thelower conveyor 20 pass, the upper edge of these belts projecting slightly from the upper surface of the table 24. This latter and thelower conveyor 20 can be lowered together, to pass from the level ofFigure 1 (corresponding to the level of the table inFigure 5.1 ), which enables thecovers 28 to be moved, to a lower level visible inFigures 6.2 and 7.2 . - The table 24 and the
lower conveyor 20 are lowered by adevice 30 comprising a pneumatic operating cylinder 32 (Figure 1 ). It should be noted that thelower conveyor 20 is driven by amotorized roller 38 which transmits its rotary movement to theconveyor 20 by friction via an idleintermediate roller 40 rigid with the table 24. Consequently, when the table 24 is lowered together with thelower conveyor 20, the transmission of movement from the motorizedroller 38 to theintermediate roller 40 ceases automatically, theconveyor 20 hence halting. - It should be noted that usual means (not shown for simplicity) are provided to vary the entry (or upstream) level of the
conveyor device 14, hence the upper edge of the upper branch of the relative belts may not be horizontal (i.e. it may be inclined upwards or downwards) to enable the covers leaving various types of conventional cover-forming machines (which have their exits at different levels) to be received directly, without varying the level at which the covers pass from theconveyor device 14 to theconveyor device 18. - In the rounding station 16 (see
Figures 2 and3 ) a die, indicated overall by 42, is present but in this specific case is incomplete in the sense that it comprises four separate portions (42.1, 42.2, 42.3, 42.4), each of which is arranged to receive one of the four corner parts of a cover 28(Figures 5.1 and 5.2 ). It should be noted that the portions (42.1-42.4) of the die 42 are shown very schematically inFigures 2 and4 , but in greater detail inFigures 5, 6 and 7 . The portions 42.1-42.4 are coplanar and aligned in opposing pairs. By virtue of arelative guide 44 provided in asupport plate 50, the two portions 42.1 and 42.3 or 42.2 and 42.4 of each pair can be moved away from or towards each other (as indicated by the double arrows B inFigure 3 ) along a bisector of a relative corner of acover 28 lying in therounding station 16. When the portions 42.1-42.4 are in their closest or working position (which is assumed just after acover 28 comes to rest - by virtue of the stop elements 36 - in the rounding station 16), therelative cover 28, or rather its corresponding corner part, lies in the situation shown byFigures 5.1 and 5.2 . Movement of the four portions 42.1-42.4 in the direction of the arrows B is achieved by relativepneumatic cylinder devices 48 fixed to theaforesaid support plate 50, which is slidable onlongitudinal guides 82 provided in aplate 84 carried by thestructure 12. As can be seen fromFigures 5, 6 and 7 , the portions 42.1-42.4 of thedie 42 are provided with an undercut 70 which enables each sharp corner of acover 28 to rest on therelative step 72. - When the table 24 is in its upper position (that of
Figures 1 and5.2 ), two stop elements 36 (Figure 3 ), symmetrically disposed one on each side of the table 24, project upwards beyond the upper surface thereof. Thestop elements 36 form part of a relative stop device indicated by 34 and rigid with the portions 42.1 and 42.2 respectively. Consequently, when these portions of thedie 42 are in their closest (working) position, the covers 28 which transit on thelower conveyor 20 interfere with thestop elements 36, to halt in therounding station 16. - For each portion 42.1-42.4 of the
die 42, themachine 10 presents a press-punch unit (one of these units is shown inFigure 4 and indicated overall by 46) carried by thestructure 12 of themachine 10. Theunit 46 comprises apress 54 and apunch 56, which are carried by asupport element 60 slidable along avertical column 58 and fixed to the lower end of thepiston rod 62 of apneumatic cylinder device 52. By operating this latter, both thepress 54 and thepunch 56 can be moved rigidly in the two senses in the direction of the double arrow C ofFigure 4 . When thecover 28 is in the position shown inFigures 5.1 and 5.2 , thepress 54 andpunch 56 can be lowered simultaneously. Thepress 54 is the first to come into contact with thecover 28, so that this latter is forced downwards. Simultaneously the table 24, together with thelower conveyor 20, is lowered to pass from its level ofFigure 5.2 to its level ofFigure 6.2 . This enables thepress 54 both to continue its downward stroke and press thecover 28 against thesunken part 66 of thedie 42, and to halt thelower conveyor 20 to prevent its belts 20.1 and 20.2 rubbing against thecover 28 and spoiling its cladding. It should be noted that the sunken part, or base, of thedie 42 is formed in this specific case by thebottom surface 66 of the relative portion 42.1-42.4 and by the upper surface of the table 24 in the situation shown inFigures 6.1 and 6.2 . As can be seen from these figures, the relative sharp corner of thecover 28 is folded upwards (as indicated by the reference numeral 29). - Between the
press 54 andsupport element 60 there is interposed an elastic element (not visible) which deforms, becoming shorter, when the thrust on thepress 54 exceeds a suitable predetermined value. In contrast, being rigidly fixed to thesupport element 60. Thepunch 56 continues its travel until it squeezes and completely flattens (as shown inFigures 7.1 and 7.2 ) the foldedcorner 29 of thecover 28. The mutual withdrawal of the four portions 42.1-42.4 and the simultaneous return of the table 24 andlower conveyor 20 to their starting position enables thecover 28, which now has rounded corners, to be extracted from thedie 42, and also enables thelower conveyor 20 to be again operated, so that this cover, no longer retained by the stop elements 36 (which have withdrawn together with the portions 42.1 and 42.2), is removed from therounding station 16 and, by the combined action of thelower conveyor 20 and the left upper conveyor 22.1 (Figure 1 ) is expelled from themachine 10, to fall for example onto aconventional conveyor device 74 which in this specific case extends transversely to themachine 10. - As the dimensions of the covers to be processed can vary within determined maximum and minimum limits, usual means are provided to adjust (by acting in this specific case on the
handwheels 78 and 80) the relative position (as indicated by the double arrows D and E) of the four portions 42.1-42.4 of thedie 42 when in their working (i.e. closest) condition. - As the thickness of the
covers 28 can also vary within determined limits, usual means (not shown in detail) are also provided to adjust the position of the upper conveyors 22.1 and 22.2 relative to the lower conveyor 20 (as indicated by the double arrows G) by acting on handwheels 86 (Figure 1 ). - From the aforegoing it is apparent that by disposing a machine of the present invention downstream of a conventional cover-forming machine in a production line for books having a cover of the initially stated type, books with a rounded-corner cover can be obtained at considerably lower costs that those incurred before using such a machine, the additional cost being essentially the cost of purchasing such a machine and of its installation and maintenance.
Claims (11)
- A machine (10) for rounding the sharp corners of hard covers (28) to be applied to books of various types, comprising:- a forming die (42) presenting a sunken part (66) having, in plan view, substantially the length and width of the sharp cornered cover (28), the sunken part of the die presenting however rounded corners (67) having the same profile as those which are to be obtained for the cover (28);- pressing means (54) for pressing the cover (28) to its full extent within the sunken part (66) of the die (42) except in the regions comprising its sharp corners, so that these latter become folded (29) outwards, the completely clad face of the cover (28) facing inwards;- punch means (56), the profile of which partly matches the profile of the rounded corners (67) of the sunken part (66) of the die (42), to press each folded corner (67) of the cover (28) against the sunken part (66) of the die (42);- means (48) for extracting the cover (28), which now presents its corners rounded, from the die (42).
- A machine (10) as claimed in claim 1, wherein the forming die (42) comprises four spaced-apart coplanar portions (42.1, 42.2, 42.3, 42.4), which each involve only one relative corner part of the cover (28).
- A machine (10) as claimed in claim 1, wherein the means for extracting the cover (28) from the die (42) consist of means (44, 48) which enable the four portions (42.1, 42.2, 42.3, 42.4) of the die (42) to be withdrawn, each in the direction of a bisector of the relative corner of the cover (28).
- A machine (10) as claimed in claim 1, wherein the forming die (42) is disposed in correspondence with a rounding station (16), there being provided means (14, 18) to feed the sharp-cornered covers (28) to the rounding station (16) one at a time and to remove therefrom the covers (28) when their corners have been rounded, and means (36) to halt one sharp-cornered cover (28) at a time in correspondence with the die (42).
- A machine (10) as claimed in claim 2, wherein the four portions (42.1, 42.2, 42.3, 42.4) can be moved away from and towards each other along the relative bisector of a corner of a cover (28).
- A machine (10) as claimed in claim 4, wherein the means for feeding and removing the covers (28) are belt conveyor devices (14, 18) comprising a first feed conveyor device (14), immediately downstream of which there is a second conveyor device (18) to bring the sharp-cornered covers (28) into correspondence with the forming die (42) and to remove, when forming has taken place, the covers (28) with rounded corners from the die (42).
- A machine (10) as claimed in claims 5 and 6, wherein the second conveyor device (18) comprises a lower conveyor (20) and two consecutive upper conveyors (22.1 and 22.2) opposite the lower conveyor (20), one (22.1) disposed upstream of the die (42) and the other (22.2) disposed downstream of the die (42), the belts (20.1 and 20.2) of the lower conveyor (20) being received in relative grooves (26) provided in the upper surface of a rigid table (24), the upper edge of the upper branch of the belts (20.1 and 20.2) projecting slightly from the upper surface of the table (24), the lower conveyor (20) and the table (24) being lowerable into alignment with the sunken part (66) of the die (42), each sharp corner of a cover (28) which has reached the rounding station (16) resting on the relative portions (42.1, 42.2, 42.3, 42.4) of the die (42).
- A machine (10) as claimed in claims 1 and 7, wherein the pressing means (54) and the punch means (56) are carried by the same support element (60), means (58, 52, 62) being provided to move the support element (60) in the two directions perpendicular to the die (42), the pressing means (54) projecting from the support element (60) such that they become the first to interfere with the cover (28) in order to force it against the sunken part (66) of the die (42), there being interposed between the pressing means (54) and the support element (60) an elastic element which shortens when the thrust on the pressing means (54) exceeds a predetermined value, the punch means (56) instead being rigidly fixed to the support element (60) and having a projection from the support element (60) which enables it to squeeze the folded corner (29) of the cover (28) after the pressing means (54) have forced the cover (28) against the sunken part (66) of the die (42).
- A machine (10) as claimed in claim 6, wherein means are provided to vary the entry level of the first conveyor device (14).
- A machine (10) as claimed in claim 7, wherein means (86) are provided to vary the distance between the lower conveyor (20) and the two upper conveyors (22.1 and 22.2) to enable covers (28) of different thicknesses to be received.
- A machine (10) as claimed in claim 5, wherein means (78. 80) are provided to vary the distance between the four portions (42.1, 42.2, 42.3, 42.4) of the die (42) when in their working position, to enable covers (28) of different plan dimensions to be received.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| SI200331679T SI1371502T1 (en) | 2002-06-14 | 2003-04-04 | Machine for rounding the corners of hard covers for books |
Applications Claiming Priority (2)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| ITMI20021332 | 2002-06-14 | ||
| ITMI20021332 ITMI20021332A1 (en) | 2002-06-14 | 2002-06-14 | MACHINE FOR ROUNDING CORNERS OF CARDBOARD COVERS BY VOLUMES |
Publications (3)
| Publication Number | Publication Date |
|---|---|
| EP1371502A2 EP1371502A2 (en) | 2003-12-17 |
| EP1371502A3 EP1371502A3 (en) | 2007-05-23 |
| EP1371502B1 true EP1371502B1 (en) | 2009-07-22 |
Family
ID=29560740
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| EP20030007728 Expired - Lifetime EP1371502B1 (en) | 2002-06-14 | 2003-04-04 | Machine for rounding the corners of hard covers for books |
Country Status (7)
| Country | Link |
|---|---|
| EP (1) | EP1371502B1 (en) |
| DE (1) | DE60328438D1 (en) |
| DK (1) | DK1371502T3 (en) |
| ES (1) | ES2329560T3 (en) |
| IT (1) | ITMI20021332A1 (en) |
| PT (1) | PT1371502E (en) |
| SI (1) | SI1371502T1 (en) |
Family Cites Families (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| US3128484A (en) * | 1961-09-08 | 1964-04-14 | Reece Folding Machine Co | Machine for making flexible book covers or similar articles |
| DE2850740C2 (en) * | 1978-11-23 | 1987-01-29 | Kolbus GmbH & Co KG, 4993 Rahden | Device for wrapping covering material around cardboard or similar flat workpieces, in particular for the production of book covers |
-
2002
- 2002-06-14 IT ITMI20021332 patent/ITMI20021332A1/en unknown
-
2003
- 2003-04-04 ES ES03007728T patent/ES2329560T3/en not_active Expired - Lifetime
- 2003-04-04 SI SI200331679T patent/SI1371502T1/en unknown
- 2003-04-04 PT PT03007728T patent/PT1371502E/en unknown
- 2003-04-04 DE DE60328438T patent/DE60328438D1/en not_active Expired - Lifetime
- 2003-04-04 DK DK03007728T patent/DK1371502T3/en active
- 2003-04-04 EP EP20030007728 patent/EP1371502B1/en not_active Expired - Lifetime
Also Published As
| Publication number | Publication date |
|---|---|
| EP1371502A3 (en) | 2007-05-23 |
| EP1371502A2 (en) | 2003-12-17 |
| PT1371502E (en) | 2009-10-19 |
| SI1371502T1 (en) | 2009-12-31 |
| ES2329560T3 (en) | 2009-11-27 |
| ITMI20021332A1 (en) | 2003-12-15 |
| DK1371502T3 (en) | 2009-11-16 |
| DE60328438D1 (en) | 2009-09-03 |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| EP0790109B1 (en) | A method and a cutting and creasing die for the production of creased and cut shapes | |
| KR100940477B1 (en) | Braille printing device | |
| CN111347717B (en) | Corrugated carton processing technology | |
| EP2080600B1 (en) | Flat bed stamping module for stamping a printed item and flat bed stamp | |
| US2141235A (en) | Process and apparatus for making arcuately plaited products | |
| GB2146281A (en) | Slit-score method and apparatus | |
| DE102007014315A1 (en) | Method of punching and sheet punching and embossing machine | |
| US5881620A (en) | Apparatus for ejecting cut corrugated board from a cutting die | |
| GB2285944A (en) | Die cutting device | |
| US5341713A (en) | Cutting apparatus for corrugated cardboard sheets | |
| DE19610574C1 (en) | Stamping and grooving tool for. e.g. cardboard mfr. | |
| EP1371502A2 (en) | Machine for rounding the corners of hard covers for books | |
| US2776610A (en) | Cutting and creasing press | |
| US4050362A (en) | Process and apparatus for blanking cardboard and the like | |
| EP1380407B1 (en) | Creasing-folding machine for cardboard sheets | |
| CA2503876A1 (en) | Stripping device for a press | |
| US3606824A (en) | Press and conveyor with self-stripping die | |
| JP2009045691A (en) | Flat plate punching machine for paper containers | |
| CN223314557U (en) | A corrugated box folding and forming device | |
| CN210795255U (en) | Single corrugated paper box cutting machine | |
| GB2121770A (en) | Pile pressing device | |
| US20050227846A1 (en) | Stripping device for a press | |
| CN112849532A (en) | Food packaging integrated equipment | |
| DE202007012350U1 (en) | Sheet punching and embossing machine | |
| CN223149864U (en) | Film feeding device of film die cutting machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| PUAI | Public reference made under article 153(3) epc to a published international application that has entered the european phase |
Free format text: ORIGINAL CODE: 0009012 |
|
| AK | Designated contracting states |
Kind code of ref document: A2 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK |
|
| PUAL | Search report despatched |
Free format text: ORIGINAL CODE: 0009013 |
|
| AK | Designated contracting states |
Kind code of ref document: A3 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: AL LT LV MK |
|
| AKX | Designation fees paid | ||
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: 8566 |
|
| 17P | Request for examination filed |
Effective date: 20080208 |
|
| RAX | Requested extension states of the european patent have changed |
Extension state: LT Payment date: 20080208 Extension state: LV Payment date: 20080208 |
|
| RBV | Designated contracting states (corrected) |
Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| GRAP | Despatch of communication of intention to grant a patent |
Free format text: ORIGINAL CODE: EPIDOSNIGR1 |
|
| GRAS | Grant fee paid |
Free format text: ORIGINAL CODE: EPIDOSNIGR3 |
|
| GRAA | (expected) grant |
Free format text: ORIGINAL CODE: 0009210 |
|
| AK | Designated contracting states |
Kind code of ref document: B1 Designated state(s): AT BE BG CH CY CZ DE DK EE ES FI FR GB GR HU IE IT LI LU MC NL PT RO SE SI SK TR |
|
| AX | Request for extension of the european patent |
Extension state: LT LV |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: FG4D |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: EP |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: FG4D |
|
| REF | Corresponds to: |
Ref document number: 60328438 Country of ref document: DE Date of ref document: 20090903 Kind code of ref document: P |
|
| RAP2 | Party data changed (patent owner data changed or rights of a patent transferred) |
Owner name: SCS AUTOMABERG SNC |
|
| REG | Reference to a national code |
Ref country code: RO Ref legal event code: EPE |
|
| REG | Reference to a national code |
Ref country code: PT Ref legal event code: SC4A Free format text: AVAILABILITY OF NATIONAL TRANSLATION Effective date: 20091009 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: T3 |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: TRGR |
|
| REG | Reference to a national code |
Ref country code: GR Ref legal event code: EP Ref document number: 20090402527 Country of ref document: GR |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FG2A Ref document number: 2329560 Country of ref document: ES Kind code of ref document: T3 |
|
| NLT2 | Nl: modifications (of names), taken from the european patent patent bulletin |
Owner name: SCS AUTOMABERG SNC Effective date: 20090923 |
|
| REG | Reference to a national code |
Ref country code: EE Ref legal event code: FG4A Ref document number: E003609 Country of ref document: EE Effective date: 20090923 |
|
| REG | Reference to a national code |
Ref country code: SK Ref legal event code: T3 Ref document number: E 6253 Country of ref document: SK |
|
| REG | Reference to a national code |
Ref country code: HU Ref legal event code: AG4A Ref document number: E006548 Country of ref document: HU |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: UEP Ref document number: 437050 Country of ref document: AT Kind code of ref document: T |
|
| PLBE | No opposition filed within time limit |
Free format text: ORIGINAL CODE: 0009261 |
|
| STAA | Information on the status of an ep patent application or granted ep patent |
Free format text: STATUS: NO OPPOSITION FILED WITHIN TIME LIMIT |
|
| 26N | No opposition filed |
Effective date: 20100423 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: MC Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 |
|
| REG | Reference to a national code |
Ref country code: CH Ref legal event code: PL |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CH Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 Ref country code: LI Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100430 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CY Free format text: LAPSE BECAUSE OF FAILURE TO SUBMIT A TRANSLATION OF THE DESCRIPTION OR TO PAY THE FEE WITHIN THE PRESCRIBED TIME-LIMIT Effective date: 20090722 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: LU Free format text: LAPSE BECAUSE OF NON-PAYMENT OF DUE FEES Effective date: 20100404 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 14 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 15 |
|
| REG | Reference to a national code |
Ref country code: FR Ref legal event code: PLFP Year of fee payment: 16 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: TR Payment date: 20220324 Year of fee payment: 20 Ref country code: SK Payment date: 20220318 Year of fee payment: 20 Ref country code: RO Payment date: 20220323 Year of fee payment: 20 Ref country code: PT Payment date: 20220322 Year of fee payment: 20 Ref country code: IT Payment date: 20220323 Year of fee payment: 20 Ref country code: EE Payment date: 20220321 Year of fee payment: 20 Ref country code: CZ Payment date: 20220323 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: NL Payment date: 20220426 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SE Payment date: 20220427 Year of fee payment: 20 Ref country code: IE Payment date: 20220427 Year of fee payment: 20 Ref country code: HU Payment date: 20220326 Year of fee payment: 20 Ref country code: GB Payment date: 20220427 Year of fee payment: 20 Ref country code: FR Payment date: 20220425 Year of fee payment: 20 Ref country code: ES Payment date: 20220503 Year of fee payment: 20 Ref country code: DK Payment date: 20220427 Year of fee payment: 20 Ref country code: DE Payment date: 20220427 Year of fee payment: 20 Ref country code: BG Payment date: 20220418 Year of fee payment: 20 |
|
| PGFP | Annual fee paid to national office [announced via postgrant information from national office to epo] |
Ref country code: SI Payment date: 20220321 Year of fee payment: 20 Ref country code: GR Payment date: 20220427 Year of fee payment: 20 Ref country code: FI Payment date: 20220427 Year of fee payment: 20 Ref country code: BE Payment date: 20220427 Year of fee payment: 20 Ref country code: AT Payment date: 20220321 Year of fee payment: 20 |
|
| REG | Reference to a national code |
Ref country code: DE Ref legal event code: R071 Ref document number: 60328438 Country of ref document: DE |
|
| REG | Reference to a national code |
Ref country code: NL Ref legal event code: MK Effective date: 20230403 |
|
| REG | Reference to a national code |
Ref country code: LT Ref legal event code: MM9A Effective date: 20230404 |
|
| REG | Reference to a national code |
Ref country code: GB Ref legal event code: PE20 Expiry date: 20230403 Ref country code: SK Ref legal event code: MK4A Ref document number: E 6253 Country of ref document: SK Expiry date: 20230404 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: CZ Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230404 |
|
| REG | Reference to a national code |
Ref country code: BE Ref legal event code: MK Effective date: 20230404 |
|
| REG | Reference to a national code |
Ref country code: ES Ref legal event code: FD2A Effective date: 20230504 |
|
| REG | Reference to a national code |
Ref country code: AT Ref legal event code: MK07 Ref document number: 437050 Country of ref document: AT Kind code of ref document: T Effective date: 20230404 |
|
| REG | Reference to a national code |
Ref country code: IE Ref legal event code: MK9A |
|
| REG | Reference to a national code |
Ref country code: SE Ref legal event code: EUG |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SI Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230405 Ref country code: GB Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230403 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: PT Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230414 Ref country code: IE Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230404 Ref country code: ES Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230405 |
|
| PG25 | Lapsed in a contracting state [announced via postgrant information from national office to epo] |
Ref country code: SK Free format text: LAPSE BECAUSE OF EXPIRATION OF PROTECTION Effective date: 20230404 |
|
| REG | Reference to a national code |
Ref country code: DK Ref legal event code: EUP Expiry date: 20230404 |